EP0392988A1 - Method of producing cylinder heads with flame plates for internal combustion engines - Google Patents
Method of producing cylinder heads with flame plates for internal combustion engines Download PDFInfo
- Publication number
- EP0392988A1 EP0392988A1 EP90830137A EP90830137A EP0392988A1 EP 0392988 A1 EP0392988 A1 EP 0392988A1 EP 90830137 A EP90830137 A EP 90830137A EP 90830137 A EP90830137 A EP 90830137A EP 0392988 A1 EP0392988 A1 EP 0392988A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- light material
- insert
- die
- casting
- head
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/24—Cylinder heads
- F02F1/26—Cylinder heads having cooling means
- F02F1/36—Cylinder heads having cooling means for liquid cooling
- F02F1/38—Cylinder heads having cooling means for liquid cooling the cylinder heads being of overhead valve type
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F7/00—Casings, e.g. crankcases
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02B—INTERNAL-COMBUSTION PISTON ENGINES; COMBUSTION ENGINES IN GENERAL
- F02B2275/00—Other engines, components or details, not provided for in other groups of this subclass
- F02B2275/26—Flame plate
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F2001/008—Stress problems, especially related to thermal stress
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/24—Cylinder heads
- F02F2001/244—Arrangement of valve stems in cylinder heads
- F02F2001/247—Arrangement of valve stems in cylinder heads the valve stems being orientated in parallel with the cylinder axis
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/24—Cylinder heads
- F02F2001/248—Methods for avoiding thermal stress-induced cracks in the zone between valve seat openings
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/24—Cylinder heads
- F02F2001/249—Cylinder heads with flame plate, e.g. insert in the cylinder head used as a thermal insulation between cylinder head and combustion chamber
Definitions
- the present invention relates in general to the so-called flame plates for the heads of internal combustion engines and more specifically concerns a method of producing such flame plates, that is, of the parts of the head which define the so-called tops of the various cylinders of the engine.
- seats are provided in the blank casting and are then filled with the material forming the insert.
- the material is integrated into the seats by fusion, sintering or, if it is preformed, by laser welding or other welding methods.
- the actual characteristics of the material forming the insert whilst improving its resistance to thermal fatigue, may be critical as regards the location and retention of the insert in the head and may also tend to disturb the propagation of heat through the critical bridge region, perhaps leading to its failure.
- the object of the present invention is to provide a method of producing flame plates of the type specified above which does not give rise to the aforementioned problems.
- a further subject of the invention is a product which can be produced by the above method.
- the solution according to the invention provides for the use of inserts of a material which has a low coefficient of expansion (typically an aluminium alloy reinforced with ceramic particles or fibres) and is therefore not very susceptible to the thermal expansion which can cause the failure of the bridge, the inserts being connected to the material forming the head by metallurgical adhesion resulting from the surface fusion of the insert during the manufacture of the head.
- a material which has a low coefficient of expansion typically an aluminium alloy reinforced with ceramic particles or fibres
- the head (cylinder head) of an internal combustion engine such as a compression-ignition (diesel) engine, is generally indicated 1 and constituted essentially by a shaped body of light material.
- light material as used in the present description and in the following claims is intended generally to mean any material (aluminium, various alloys) currently known as a "light alloy” and used for manufacturing heads for internal combustion engines, this choice of term being intended to leave out of consideration either whether the material is an alloy proper or the composition thereof, which are irrelevant for the purposes of the invention.
- the embodiment illustrated is the head 1 of a compression-ignition (diesel) engine including four cylinders with respective top regions defining the so-called flame plates of the head.
- the head 1 is provided with two holes 2 for defining the valve-mounting seats.
- the inserts are of aluminium alloy reinforced with fibres (whiskers) or particles of ceramics material.
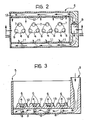
- the head 1 is produced by casting in a die (mould), generally indicated 5 in Figures 2 and 3.
- the die 5 is substantially comparable to a tank with a base wall from which formations (rods) project upwardly for reproducing, in a complementary manner, the shapes of the holes 2 and 3 described above.
- each cylinder there are two main rods 6 for defining the holes 2 and a third rod 7 for defining the hole 3.
- the inserts 4 are made so that they can be fitted onto the rods 6 and 7 and remain at a certain distance (for example, of the order of 1.5-2.5 mm) from the upper face of the base wall of the die 5.
- Ducts are provided in the die 5 for distributing the casting material beneath the base wall, the ducts branching from a main opening 9 situated at the upper end of the die for the introduction of the casting material (light material - as defined above).
- the distribution ducts 8 open into the die through respective openings 11, 12 situated on the two opposite sides of the die (see particularly the plan view of Figure 2).
- the openings for distributing the casting material over the two walls are arranged in staggered positions.
- one side of the die has as many openings 11 as there are cylinders of the head 1. There are therefore four openings, each situated in alignment with the axis of one of the cylinders, that is, aligned with the centre line between the main rods 6 and thus oriented axially of the corresponding cylinder.
- Openings 12 are provided on the opposite side, of which the central three are in positions intermediate two adjacent cylinders whilst the two end openings are adjacent the end parts of the die 5. All the openings 12 are thus oriented tangentially of at least one corresponding cylinder of the head 1.
- the die or mould 6 is initially brought to a temperature of not less than 300°C.
- the inserts 4 are then fitted onto the rod 6, 7, care being taken that the space or gap defined with respect to the base of the die has the prescribed dimensions (from 1.5 to 2.5 mm).
- the surface of the insert 4 must be activated appropriately before casting by means of sandblasting or at any rate by treatments for removing the surface layer of alumina which is always present on this type of material.
- the die is then closed and the light material necessary for making the head introduced through the feed opening 9.
- the material is cast at a temperature of at least 700°C (preferably about 750°C) and is propagated within the die 5, particularly over the entire surfaces of the inserts 4.
- the immediate heating of the entire surfaces of the latter causes the surface fusion of the inserts 4 and their intimate adhesion to the mass of light material forming the head.
- the die 5 is then cooled according to known criteria, so as to cool the head which is then removed from the die.
- the head undergoes mechanical working (levelling) with the primary object of removing the mass of light material which is introduced into the gap or space, indicated 13, between the inserts 4 and the base wall of the die.
- the working in question causes the inserts 4 to reappear at the outer surface of the head.
- the mechanical working of the whole head is then carried out (by known techniques) so as, for example, to bring the holes 2 for forming the valve-mounting seats to the required tolerance.
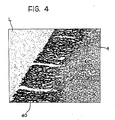
- Figure 4 shows the microstructural appearance of the interface region between the material of one of the inserts 4 and the mass of light material of the head, generally indicated L.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Combustion & Propulsion (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Cylinder Crankcases Of Internal Combustion Engines (AREA)
Abstract
Description
- The present invention relates in general to the so-called flame plates for the heads of internal combustion engines and more specifically concerns a method of producing such flame plates, that is, of the parts of the head which define the so-called tops of the various cylinders of the engine.
- It is known that the resistance of these flame plates to thermal fatigue, particularly in heads of light material intended for compression-ignition (diesel) engines, can be improved by inserting an insert of a material with an increased resistance to the thermal stresses generated during the operation of the engine in the bridge region (that is, in the region which separates the holes defining the valve seats and any hole for the insertion of an injector).
- A solution of this type is described, for example, in United States
Patent 4, 487,175. - Various techniques have hitherto been adopted for locating the insert and ensuring that it is firmly retained in the material forming the head.
- According to a solution which can be adopted for inserts made from steel plates or small inserts of alloy material, it is known to locate the insert in the die (mould) for casting the head so that the insert is incorporated in the material of the head and a mechanical anchorage is thus achieved.
- According to a possible alternative, seats are provided in the blank casting and are then filled with the material forming the insert. The material is integrated into the seats by fusion, sintering or, if it is preformed, by laser welding or other welding methods.
- These solutions cannot be considered wholly satisfactory. In general, the actual characteristics of the material forming the insert, whilst improving its resistance to thermal fatigue, may be critical as regards the location and retention of the insert in the head and may also tend to disturb the propagation of heat through the critical bridge region, perhaps leading to its failure.
- The object of the present invention is to provide a method of producing flame plates of the type specified above which does not give rise to the aforementioned problems.
- According to the present invention, this object is achieved by virtue of a method which has the characteristics quoted specifically in the following claims.
- A further subject of the invention is a product which can be produced by the above method.
- By way of summary, the solution according to the invention provides for the use of inserts of a material which has a low coefficient of expansion (typically an aluminium alloy reinforced with ceramic particles or fibres) and is therefore not very susceptible to the thermal expansion which can cause the failure of the bridge, the inserts being connected to the material forming the head by metallurgical adhesion resulting from the surface fusion of the insert during the manufacture of the head.
- The invention will now be described, purely by way of non-limiting example, with reference to the appended drawings, in which:
- Figure 1 shows schematically, in a general perspective view, the head of an internal combustion engine produced according to the invention,
- Figure 2 is a view from above of a die (mould) usable for carrying out the invention,
- Figure 3 is a section taken on the line III-III of Figure 2, and
- Figure 4 reproduces a view through a microscope, showing the intimate adhesion at a metallurgical level of two component parts of a head according to the invention.
- In Figure 1, the head (cylinder head) of an internal combustion engine, such as a compression-ignition (diesel) engine, is generally indicated 1 and constituted essentially by a shaped body of light material.
- The term "light material" as used in the present description and in the following claims is intended generally to mean any material (aluminium, various alloys) currently known as a "light alloy" and used for manufacturing heads for internal combustion engines, this choice of term being intended to leave out of consideration either whether the material is an alloy proper or the composition thereof, which are irrelevant for the purposes of the invention.
- The embodiment illustrated is the head 1 of a compression-ignition (diesel) engine including four cylinders with respective top regions defining the so-called flame plates of the head.
- In correspondence with each cylinder, the head 1 is provided with two holes 2 for defining the valve-mounting seats. The holes 2, together with a
further hole 3 for housing an injector, define the so-called bridge region in which aninsert 4 of a material with good resistance to thermal stresses is located. - According to the solution currently considered preferable, the inserts are of aluminium alloy reinforced with fibres (whiskers) or particles of ceramics material.
- According to a known solution, the head 1 is produced by casting in a die (mould), generally indicated 5 in Figures 2 and 3.
- In general terms, the die 5 is substantially comparable to a tank with a base wall from which formations (rods) project upwardly for reproducing, in a complementary manner, the shapes of the
holes 2 and 3 described above. - More precisely, in correspondence with each cylinder, there are two
main rods 6 for defining the holes 2 and a third rod 7 for defining thehole 3. - The
inserts 4 are made so that they can be fitted onto therods 6 and 7 and remain at a certain distance (for example, of the order of 1.5-2.5 mm) from the upper face of the base wall of thedie 5. - Ducts, generally indicated 8, are provided in the
die 5 for distributing the casting material beneath the base wall, the ducts branching from a main opening 9 situated at the upper end of the die for the introduction of the casting material (light material - as defined above). - The
distribution ducts 8 open into the die throughrespective openings - The openings for distributing the casting material over the two walls are arranged in staggered positions.
- In the embodiment illustrated, one side of the die has as
many openings 11 as there are cylinders of the head 1. There are therefore four openings, each situated in alignment with the axis of one of the cylinders, that is, aligned with the centre line between themain rods 6 and thus oriented axially of the corresponding cylinder. - Five
openings 12 are provided on the opposite side, of which the central three are in positions intermediate two adjacent cylinders whilst the two end openings are adjacent the end parts of thedie 5. All theopenings 12 are thus oriented tangentially of at least one corresponding cylinder of the head 1. - This solution, together with the presence of the above-described space or gap beneath each
insert 4, has been shown to be preferable for achieving the best distribution of the casting material. - According to the currently-preferred embodiment of the invention, the die or
mould 6 is initially brought to a temperature of not less than 300°C. - The
inserts 4 are then fitted onto therod 6, 7, care being taken that the space or gap defined with respect to the base of the die has the prescribed dimensions (from 1.5 to 2.5 mm). - Usually, the surface of the
insert 4 must be activated appropriately before casting by means of sandblasting or at any rate by treatments for removing the surface layer of alumina which is always present on this type of material. - The die is then closed and the light material necessary for making the head introduced through the feed opening 9. The material is cast at a temperature of at least 700°C (preferably about 750°C) and is propagated within the
die 5, particularly over the entire surfaces of theinserts 4. The immediate heating of the entire surfaces of the latter causes the surface fusion of theinserts 4 and their intimate adhesion to the mass of light material forming the head. - The die 5 is then cooled according to known criteria, so as to cool the head which is then removed from the die.
- At this point, the head undergoes mechanical working (levelling) with the primary object of removing the mass of light material which is introduced into the gap or space, indicated 13, between the
inserts 4 and the base wall of the die. In other words, the working in question causes theinserts 4 to reappear at the outer surface of the head. - The mechanical working of the whole head is then carried out (by known techniques) so as, for example, to bring the holes 2 for forming the valve-mounting seats to the required tolerance.
- It has been shown that the casting technique described is decisive for the production of an intimate and firm anchorage between the
inserts 4 and the mass of light material forming the head as a whole 1. - Figure 4 shows the microstructural appearance of the interface region between the material of one of the
inserts 4 and the mass of light material of the head, generally indicated L. - In the image (magnified 100 times) the presence of a region of surface fusion of the insert, indicated 40, which can give rise to a practically inseparable metallurgical adhesion between the
insert 4 and the rest of the head 1, can clearly be recognised. - It has been found that the best results from the qualitative point of view are obtained when the dimensions of the
inserts 4 are such that the ratio between their mass and the overall mass of the head is of the order of 1:1000 (for example, 15 grams/mass for theinserts 5 in comparison with 15 kg overall mass of the head 1).
Claims (22)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT6727489 | 1989-04-13 | ||
| IT8967274A IT1232718B (en) | 1989-04-13 | 1989-04-13 | PROCEDURE FOR MAKING THE SO-CALLED FLAME-PLATES OF HEADS FOR INTERNAL COMBUSTION ENGINES AND THEIR PRODUCT |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0392988A1 true EP0392988A1 (en) | 1990-10-17 |
| EP0392988B1 EP0392988B1 (en) | 1995-08-16 |
Family
ID=11301055
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP90830137A Expired - Lifetime EP0392988B1 (en) | 1989-04-13 | 1990-04-03 | Method of producing cylinder heads with flame plates for internal combustion engines |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0392988B1 (en) |
| BR (1) | BR9001776A (en) |
| DE (1) | DE69021614T2 (en) |
| IT (1) | IT1232718B (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2003006811A1 (en) * | 2001-07-11 | 2003-01-23 | Mahle Ventiltrieb Gmbh | Insert, acting as the base area of a cylinder head |
| WO2017082846A1 (en) | 2015-11-11 | 2017-05-18 | Ford Otomotiv Sanayi A. S. | Multi-piece cylinder head |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10353473B4 (en) * | 2003-11-15 | 2007-02-22 | Daimlerchrysler Ag | Component of an internal combustion engine and method for its production |
| DE102004001908A1 (en) * | 2004-01-14 | 2005-08-04 | Daimlerchrysler Ag | Cylinder head for a liquid-cooled internal combustion engine with gas change channels, cooling agent space around the channels and bracing elements in the cylinder head made of stronger material than the material surrounding the head |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4487175A (en) * | 1981-01-13 | 1984-12-11 | Kl/o/ ckner-Humboldt-Deutz AG | Cylinder head for internal combustion engine |
| US4604779A (en) * | 1984-02-27 | 1986-08-12 | Ngk Spark Plug Co., Ltd. | Method of producing a cylinder head with a port liner |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB892770A (en) * | 1959-05-04 | 1962-03-28 | Hepworth & Grandage Ltd | Improvements in or relating to casting aluminium or aluminium alloys on to ferrous metals |
| US4546048A (en) * | 1984-03-23 | 1985-10-08 | Dana Corporation | Composite thermal shield for engine components |
-
1989
- 1989-04-13 IT IT8967274A patent/IT1232718B/en active
-
1990
- 1990-04-03 DE DE69021614T patent/DE69021614T2/en not_active Expired - Fee Related
- 1990-04-03 EP EP90830137A patent/EP0392988B1/en not_active Expired - Lifetime
- 1990-04-10 BR BR909001776A patent/BR9001776A/en not_active IP Right Cessation
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4487175A (en) * | 1981-01-13 | 1984-12-11 | Kl/o/ ckner-Humboldt-Deutz AG | Cylinder head for internal combustion engine |
| US4604779A (en) * | 1984-02-27 | 1986-08-12 | Ngk Spark Plug Co., Ltd. | Method of producing a cylinder head with a port liner |
Non-Patent Citations (1)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 9, no. 111 (M-379)(1834) 15 May 1985, & JP-A-59 231163 (YAMAHA HADSUDOKI K.K.) 25 December 1984, * |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2003006811A1 (en) * | 2001-07-11 | 2003-01-23 | Mahle Ventiltrieb Gmbh | Insert, acting as the base area of a cylinder head |
| WO2017082846A1 (en) | 2015-11-11 | 2017-05-18 | Ford Otomotiv Sanayi A. S. | Multi-piece cylinder head |
Also Published As
| Publication number | Publication date |
|---|---|
| DE69021614D1 (en) | 1995-09-21 |
| BR9001776A (en) | 1991-06-04 |
| IT1232718B (en) | 1992-03-04 |
| EP0392988B1 (en) | 1995-08-16 |
| IT8967274A0 (en) | 1989-04-13 |
| DE69021614T2 (en) | 1996-01-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0796687B1 (en) | A method for producing a piston for an internal combustion engine and a piston produced by the method | |
| EP0445355B1 (en) | Cylinder head casting apparatus and method | |
| US5979298A (en) | Cooling gallery for pistons | |
| US7198026B2 (en) | Divider plate for an inlet port, sand core for forming an inlet port, and cylinder head | |
| US5361823A (en) | Casting core and method for cast-in-place attachment of a cylinder liner to a cylinder block | |
| GB2185925A (en) | Vented casting molds | |
| JP3668209B2 (en) | Engine block casting | |
| US4939984A (en) | Investment-cast piston crown cap with encapsulated non-metallic insulating core | |
| JP3676759B2 (en) | Engine block casting | |
| JP2003080346A (en) | Engine block casting method | |
| EP0410612B1 (en) | Heat-insulating structure of swirl chamber | |
| US4577600A (en) | Structure of divided combustion chamber for diesel engine | |
| EP0392988B1 (en) | Method of producing cylinder heads with flame plates for internal combustion engines | |
| GB2352418A (en) | Water jacket core | |
| US4252175A (en) | Cylinder block having a cast-in core unit and process for manufacturing same | |
| JP2003048050A (en) | Engine block casting method | |
| US5445210A (en) | Casting core for forming cast-in intersecting push rod passages and oil gallery within a cylinder block | |
| US5010861A (en) | Heat-insulating structure of swirl chamber and production method thereof | |
| EP1143135B1 (en) | Cooling water channel structure of a cylinder head and method of manufacturing a cylinder head | |
| JPS61126943A (en) | Chaplet for casting cylinder block | |
| CN105934578B (en) | Engine block for diesel engine with one-piece cylinder head and casting method thereof | |
| US2893371A (en) | Expansion joint | |
| JPH0780032B2 (en) | Disappearance model for casting cylinder heads for internal combustion engines. | |
| JPH0780033B2 (en) | Disappearance model for casting cylinder heads for internal combustion engines. | |
| US5474119A (en) | Method of and mold for casting a combined engine block and cylinder head for a twin piston engine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB SE |
|
| 17P | Request for examination filed |
Effective date: 19900925 |
|
| 17Q | First examination report despatched |
Effective date: 19920511 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19950816 |
|
| REF | Corresponds to: |
Ref document number: 69021614 Country of ref document: DE Date of ref document: 19950921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19951116 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19990323 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000403 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20000403 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20010321 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20010430 Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021231 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |