EP0376773B1 - Dispositif pour détecter, au cours du soudage, des variations dans l'état physique de la matière plastique d'une pièce de raccordement prévue pour la jonction de tubes - Google Patents
Dispositif pour détecter, au cours du soudage, des variations dans l'état physique de la matière plastique d'une pièce de raccordement prévue pour la jonction de tubes Download PDFInfo
- Publication number
- EP0376773B1 EP0376773B1 EP19890403330 EP89403330A EP0376773B1 EP 0376773 B1 EP0376773 B1 EP 0376773B1 EP 19890403330 EP19890403330 EP 19890403330 EP 89403330 A EP89403330 A EP 89403330A EP 0376773 B1 EP0376773 B1 EP 0376773B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cavity
- connection part
- resistor
- heating
- cavities
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000003466 welding Methods 0.000 title claims abstract description 19
- 239000012815 thermoplastic material Substances 0.000 title 1
- 239000000463 material Substances 0.000 claims abstract description 39
- 238000010438 heat treatment Methods 0.000 claims abstract description 31
- 239000012768 molten material Substances 0.000 claims description 11
- 238000000034 method Methods 0.000 claims description 5
- 239000000155 melt Substances 0.000 claims description 4
- 229920001187 thermosetting polymer Polymers 0.000 claims 3
- 229920003023 plastic Polymers 0.000 abstract description 9
- 239000004033 plastic Substances 0.000 abstract description 9
- 230000008878 coupling Effects 0.000 abstract 1
- 238000010168 coupling process Methods 0.000 abstract 1
- 238000005859 coupling reaction Methods 0.000 abstract 1
- 239000012943 hotmelt Substances 0.000 description 4
- 230000035515 penetration Effects 0.000 description 4
- 238000004804 winding Methods 0.000 description 4
- 230000000694 effects Effects 0.000 description 3
- 239000004698 Polyethylene Substances 0.000 description 2
- 238000001816 cooling Methods 0.000 description 2
- 230000004927 fusion Effects 0.000 description 2
- -1 polyethylene Polymers 0.000 description 2
- 229920000573 polyethylene Polymers 0.000 description 2
- 230000002028 premature Effects 0.000 description 2
- 206010013647 Drowning Diseases 0.000 description 1
- 238000007792 addition Methods 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000000470 constituent Substances 0.000 description 1
- 230000010339 dilation Effects 0.000 description 1
- 238000005485 electric heating Methods 0.000 description 1
- 230000001939 inductive effect Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 238000012544 monitoring process Methods 0.000 description 1
- 210000003739 neck Anatomy 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/34—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement"
- B29C65/3404—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement" characterised by the type of heated elements which remain in the joint
- B29C65/342—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement" characterised by the type of heated elements which remain in the joint comprising at least a single wire, e.g. in the form of a winding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/34—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement"
- B29C65/3468—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement" characterised by the means for supplying heat to said heated elements which remain in the join, e.g. special electrical connectors of windings
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/05—Particular design of joint configurations
- B29C66/10—Particular design of joint configurations particular design of the joint cross-sections
- B29C66/11—Joint cross-sections comprising a single joint-segment, i.e. one of the parts to be joined comprising a single joint-segment in the joint cross-section
- B29C66/112—Single lapped joints
- B29C66/1122—Single lap to lap joints, i.e. overlap joints
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/50—General aspects of joining tubular articles; General aspects of joining long products, i.e. bars or profiled elements; General aspects of joining single elements to tubular articles, hollow articles or bars; General aspects of joining several hollow-preforms to form hollow or tubular articles
- B29C66/51—Joining tubular articles, profiled elements or bars; Joining single elements to tubular articles, hollow articles or bars; Joining several hollow-preforms to form hollow or tubular articles
- B29C66/52—Joining tubular articles, bars or profiled elements
- B29C66/522—Joining tubular articles
- B29C66/5221—Joining tubular articles for forming coaxial connections, i.e. the tubular articles to be joined forming a zero angle relative to each other
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/73—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/739—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/7392—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic
- B29C66/73921—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic characterised by the materials of both parts being thermoplastics
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/91—Measuring or controlling the joining process by measuring or controlling the temperature, the heat or the thermal flux
- B29C66/914—Measuring or controlling the joining process by measuring or controlling the temperature, the heat or the thermal flux by controlling or regulating the temperature, the heat or the thermal flux
- B29C66/9161—Measuring or controlling the joining process by measuring or controlling the temperature, the heat or the thermal flux by controlling or regulating the temperature, the heat or the thermal flux by controlling or regulating the heat or the thermal flux, i.e. the heat flux
- B29C66/91651—Measuring or controlling the joining process by measuring or controlling the temperature, the heat or the thermal flux by controlling or regulating the temperature, the heat or the thermal flux by controlling or regulating the heat or the thermal flux, i.e. the heat flux by controlling or regulating the heat generated by Joule heating or induction heating
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16L—PIPES; JOINTS OR FITTINGS FOR PIPES; SUPPORTS FOR PIPES, CABLES OR PROTECTIVE TUBING; MEANS FOR THERMAL INSULATION IN GENERAL
- F16L47/00—Connecting arrangements or other fittings specially adapted to be made of plastics or to be used with pipes made of plastics
- F16L47/02—Welded joints; Adhesive joints
- F16L47/03—Welded joints with an electrical resistance incorporated in the joint
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/34—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement"
- B29C65/3472—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement" characterised by the composition of the heated elements which remain in the joint
- B29C65/3476—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using heated elements which remain in the joint, e.g. "verlorenes Schweisselement" characterised by the composition of the heated elements which remain in the joint being metallic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/71—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the composition of the plastics material of the parts to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/94—Measuring or controlling the joining process by measuring or controlling the time
- B29C66/944—Measuring or controlling the joining process by measuring or controlling the time by controlling or regulating the time
Definitions
- the subject of the invention is a device intended to detect, during its heating, variations in the physical state of the heat-sealable plastic material of a connecting piece intended to be welded with another piece of the same material in the form of tube with circular or substantially circular section.
- plastic tubes are used more and more frequently and particularly polyethylene.
- connection piece which may in particular consist of a sleeve serving to connect one end of two tubes, or even, for example, in a connection socket having locally the shape of a saddle and allowing the transverse connection of the tubes.
- the connecting piece chosen it usually comprises, in its thickness, an electric heating resistor arranged near its surface which must come into contact with that of the tube.
- the welding operation is carried out by connecting the resistor to an electrical source (such as a rectified alternating current source) which, by the Joule effect, will heat the resistance and cause softening with fusion of the surrounding plastic, thus achieving the welding.
- thermoprobe a microswitch sensitive to the pressure of the softened material within the cavity
- sensor sensitive to hardness or consistency. of this same material.
- the object of the invention is to solve these various problems by defining conditions for shape, size and position of the cavities into which the softened material penetrates during heating and at which the sensors detect variations in its physical state.
- the invention is characterized first of all in that the aforementioned minimum radial distance h1 and the dimensioning d in section, along a plane substantially perpendicular to its axis, of the cavity of the connecting piece close to its wall bottom, are each selected to be less than or equal to the predetermined radial thickness of molten material e measured from said resistance to the outer surface of said connecting piece.
- the invention further provides that the radial distance h1 has a value substantially equal to that of the predetermined radial thickness of material which melts during the heating of said parts before a pressure of expansion induced by the heating causes the penetration of said melt in the cavity, over a radial thickness e - h1.
- part of the resistor which is closest to the bottom wall of the cavity must be interpreted as defining the zone of the resistor which is located closest to the bottom wall of this cavity and substantially opposite it.
- the cavity in question will widen beyond its bottom wall by locally presenting a shoulder such that the distance which separates this shoulder from the part of the resistance closest to this wall of bottom is less than or equal to twice the thickness of the material of the part where the cavity is formed and which has softened during heating.
- the implementation conditions imposed by the invention are as follows: 0 ⁇ d ⁇ (0.03. ⁇ ) + 8 and 0 ⁇ h1 ⁇ (0.03. ⁇ ) + 8 with d: diameter expressed in mm of the aforementioned cavity near its bottom wall, h1 : distance expressed in mm between the bottom wall of this same cavity and the part closest to the heating resistance ⁇ : diameter expressed in mm of the orifice of the sleeve.
- a plastic connection piece hot-melt such as polyethylene, this piece forming a sleeve in the orifice 2 of which the ends, respectively 3a, 4a of two circular cylindrical tubes 3, 4 also engage in hot-melt plastic.
- the tubes 3 and 4 are arranged coaxially, substantially in the axis 2a of the orifice of the sleeve and have an outside diameter slightly smaller than the diameter ⁇ of the orifice 2, so that the sleeve and the tubes have corresponding surfaces in vis-à-vis by which they will be able to be mutually connected during welding.
- the sleeve 1 For joining the tubes, the sleeve 1 includes an electrical heating resistance 5 embedded in its thickness, in the immediate vicinity of its interior surface marked 1a.
- the resistor 5 is connected by its terminals 6a, 6b to a source of electrical energy (not shown) capable of ensuring a sufficient rise in the temperature of the resistor to induce the welding of the parts together.
- the resistor 5 is constituted by a cylindrical electric winding with a circular section of axis parallel to that of the sleeve and connected to the above-mentioned electric source.
- the connecting piece 1 is also equipped with two sensors 7, 8 arranged in cavities 9, 10 each directed along an axis 9a, 10a substantially radial to that 2a of the tubes, these cavities extending up to in the vicinity of the closest neighboring portion of the winding, ending at the same level with a bottom wall 11 which can be distinguished more clearly in FIGS. 2 to 4 (in which for the sake of clarity is shown cavities without sensor).
- the sensors 7, 8, known per se can for example consist of microswitches.
- the process welding parts is usually such that once sufficient heating of the resistance is obtained, the plastic material which surrounds it melts and expands, inducing under the effect of this expansion pressure, a penetration of softened material in the bottom cavities 9 and 10 then, this dilation continuing, a rise of material in the cavities until this material comes to exert on the sensors 7 and 8 an action tending to cause an interruption in the supply of electrical energy to the heating resistor, thereby interrupting the heating of the parts which are then allowed to cool.
- the invention therefore first of all provides for placing the bottom 11 of the cavities at such a distance from the part of the closest heating resistor that the bottom 11 in question is melted under the effect of heating. before the expansion pressure is sufficient to push the molten material into the cavities.
- h 1 must be less than or equal to e with: h 1: average distance between the bottom 11 of each cavity and the general plane 15 tangent to the winding and in which extends the part of the resistance which is closest to said bottom, and e : thickness of constituent plastic of the sleeve 1 which melts during the heating of the parts.
- this thickness e corresponds to the thickness of material situated, relative to the axis of the sleeve, beyond, or outside, the plane 15.
- the invention further provides for controlling the speed of flow of the material by a rigorous conformation of the cavities so that their dimensioning in section is, at least near their bottom and along a plane substantially perpendicular to their axis (such as 9a in Figure 2), less than or equal to the above thickness e of softened material.
- this sudden widening of section will be located at a distance h2 from the general plane 15 defined above such that h2 ⁇ 2nd , (e being always the aforementioned thickness of molten material).
- Figure 3 for example is illustrated a cavity having the appearance of two adjoining cylinders of circular section having successively, starting from the bottom 11, a diameter d then a diameter D with D> d.
- FIG 4 there is shown another alternative embodiment in which the cavity is in the form of two cylinders with circular section of diameter respective d and D joined by a truncated cone whose small base is located at the distance h2 from the plane 15 of the resistor 5.
- connection pieces other than sleeves such as for example connection sockets having locally the form of a saddle overlapping the outer surface of a tube for its connection with another tube arranged transversely.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
Description
- L'invention a pour objet un dispositif destiné à détecter, au cours de son chauffage, des variations dans l'état physique de la matière plastique thermosoudable d'une pièce de raccordement prévue pour être soudée avec une autre pièce de même matière en forme de tube à section circulaire ou sensiblement circulaire.
- Pour de nombreux emplois, et en particulier pour l'établissement de réseaux de distribution de gaz, on utilise aujourd'hui de plus en plus fréquemment des tubes en matière plastique et particulièrement en polyéthylène.
- L'assemblage de ces tubes ne pouvant en pratique se faire de façon satisfaisante par coilage, on est donc amené à les souder et plus précisément à les thermosouder.
- Pour ce faire, on a généralement recours à une pièce de raccordement qui peut notamment consister en un manchon servant à relier l'une des extrémités de deux tubes, ou encore, par exemple, en une prise de branchement ayant localement la forme d'une selle et permettant le raccordement transversal des tubes. Quelle que soit la pièce de raccordement choisie, celle-ci comporte de façon habituelle, dans son épaisseur, une résistant électrique de chauffage disposée à proximité de sa surface qui doit venir en contact de celle du tube. L opération de soudage est réalisée en raccordant la résistance à une source électrique(telle qu'une source de courant alternatif redressé) qui, par effet Joule, va échauffer la résistance et provoquer le ramollissement avec fusion de la matière plastique environnante, réalisant ainsi le soudage.
- Pour avantageuse qu'elle soit, une telle technique d'assemblage présente cependant une difficulté, à savoir le contrôle du temps de chauffage de la résistance nécessaire à l'obtention d'une soudure de bonne qualité et donc à la formation d'un bloc unitaire entre le(les) tube(s) et la pièce de raccordement.
- On sait aujourd'hui qu'un tel contrôle peut être effectue de façon satisfaisante essentiellement par le suivi de deux grandeurs physiques : la température et le volume de la matière constitutive des pièces à souder.
- Pour réaliser le contrôle actif de ces paramètres, il a été proposé de ménager dans l'une des pièces à assembler au moins une cavité au sein de laquelle la matière ramollie est susceptible de pénétrer, cette cavité s'étendant, selon un axe sensiblement radial au(x) tube(s), jusqu'au voisinage d'une partie de la résistance en se terminant par une paroi de fond. A cette cavité est adjoint un capteur propre à capter, au sein de cette dernière, des variations dans l'état physique de la matière, ce capteur étant en général associé à des moyens propres à commander la coupure de l'alimentation en énergie électrique de la résistance de chauffage.
- Différents types de capteurs ont d'ailleurs déjà été envisagés, tels par exemple qu'une thermosonde, un micro-interrupteur sensible à la pression de la matière ramollie au sein de la cavité, ou encore un capteur sensible à la dureté ou à la consistance de cette même matière.
- De tels capteurs et d'autres sont notamments décrits dans la demande de brevet français FR-A-2555936 et ses certificats d'additions FR-A- 2572327 et FR-A-2600008, ou encore dans la demande EP-A-0149410 qui décrit un dispositif comprenant :
- une pièce de raccordement prévue pour être soudée autour d'au moins une autre pièce tubulaire en matière plastique thermofusible, lesdites pièces présentant des surfaces respectivement intérieure et extérieure par lesquelles elles sont mutuellement reliées au cours du soudage, au moins une cavité au sein de laquelle la matière ramollie est susceptible de pénétrer étant ménagée dans ladite pièce de raccordement, cette cavité s'étendant suivant un axe sensiblement radial à la pièce tubulaire et à ladite pièce de raccordement, en se terminant par une paroi de fond adjacente à ladite surface intérieure de la pièce de raccordement,
- une résistance électrique de chauffage noyée dans la pièce de raccordement entre sadite surface intérieure et ladite cavité, à une distance radiale minimum donnée (h₁) de ladite paroi de fond de la cavité, ladite résistance étant connectable à une source électrique pour faire fondre ladite matière thermofusible sur une épaisseur radiale prédéterminée de matière fondue en vue du soudage entre elles desdites pièces,
- et au moins un capteur disposé dans ladite cavité pour y capter des variations d'état physique de la matière.
- Malgré cela, certains problèmes restent encore posés et la qualité de soudage des pièces n'est pas toujours satisfaisante.
- En particulier, différents essais ont montré que pour des jeux d'assemblage réduits entre les pièces, le temps de soudage a tendance à diminuer alors que les jeux augmentent, ce qui comme on le comprend, nuit sérieusement à la qualité de la soudure.
- Or, dans la pratique, les jeux d'assemblage peuvent varier de façon importante suivant les pièces utilisées.
- De plus, les techniques actuelles de soudage ne permettent pas d'obtenir dans de bonnes conditions que l'épaisseur de matière fondue au cours du chauffage augmente avec la taille des pièces à assembler ce qui est en pratique nécessaire.
- L'invention a pour objet de résoudre ces différents problèmes en définissant des conditions de forme, de dimension et de position des cavités dans lesquelles la matière ramollie pénètre au cours du chauffage et au niveau desquelles les capteurs relèvent les variations de son état physique.
- Pour cela, l'invention se caractérise tout d'abord en ce que la distance radiale minimum précitée h₁ et le dimensionnement d en section, suivant un plan sensiblement perpendiculaire à son axe, de la cavité de la pièce de raccordement à proximité de sa paroi de fond, sont chacun sélectionnés pour être inférieurs ou égaux à l'épaisseur radiale prédéterminée de matière fondue e mesurée depuis ladite résistance vers la surface extérieure de ladite pièce de raccordement.
- Avantageusement, l'invention prévoit par surcroît que la distance radiale h₁ ait une valeur sensiblement égale à celle de l'épaisseur radiale prédéterminée de matière qui fond lors du chauffage desdites pièces avant qu'une pression de dilatation induite par le chauffage provoque la pénétration de ladite matière fondue dans la cavité, sur une épaisseur radiale e - h₁.
- Ainsi, on pourra assurer le ramolissement avec fusion du fond de la cavité avant que la pression de la matière fondue par la résistance soit suffisante pour "le rompre", tout en évitant qu'une pénétration prématurée de matière fondue dans la cavité conduise le capteur à commander l'interruption de l'alimentation en énergie électrique de la résistance avant que la cohésion des pièces, au niveau de leur interface de soudage, soit suffisante pour assurer, après refroidissement, une soudure de bonne qualité.
- On notera dès à présent que l'expression "partie de la résistance qui est la plus proche de la paroi de fond de la cavité" doit s'interpréter comme définissant la zone de la résistance qui est située au plus près de la paroi de fond de cette cavité et sensiblement en regard de celle-ci.
- Selon une autre caractéristique de l'invention, la cavité en question s'élargira au-delà de sa paroi de fond en présentant localement un épaulement tel que la distance qui sépare cet épaulement de la partie de la résistance la plus proche de cette paroi de fond soit inférieure ou égale au double de l'épaisseur de matière constitutive de la pièce où est ménagée la cavité et qui s'est ramollie au cours du chauffage.
- Ainsi, la plupart des capteurs existant actuellement pourront- ils être disposés dans la cavité avec des conditions optimales de mise en place, permettant un contrôle tout à fait rigoureux du temps de chauffage.
- Même si l'invention peut être appliquée pour assurer l'assemblage de différents types de raccordement et de différentes pièces tubulaires, il reste malgré tout qu'actuellement, dans la pratique, un grand nombre d'interventions consistent en le soudage de deux tubes mis bout à bout et enfilés, à l'une de leurs extrémités, à l'intérieur d'un manchon de raccordement pourvu d'un orifice de réception à section circulaire.
- Les conditions de mise en oeuvre qu'imposent alors l'invention sont les suivantes :

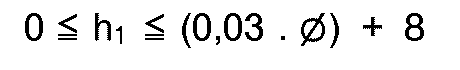
avec d : diamètre exprimé en mm de la cavité précitée à proximité de sa paroi de fond,
h₁ : distance exprimée en mm entre la paroi de fond de cette même cavité et la partie la plus voisine de la résistance de chauffage
⌀ : diamètre exprimé en mm de l'orifice du manchon. - L'invention, ses caractéristiques et avantages apparaîtront plus clairement de la description qui va suivre faite en référence aux dessins annexés dans lesquels :
- la figure 1 est une vue en coupe longitudinale de deux tubes disposés coaxialement, prêts à être réunis par l'intermédiaire d'un manchon de raccordement électrosoudable,
- la figure 2 est une vue agrandie du détail repéré II à la figure 1,
- et les figures 3 et 4 sont deux variantes possibles de réalisation de la cavité illustrée figure 2.
- Si l'on se reporte tout d'abord à la figure 1, on voit illustrer une pièce de raccordement en matière plastique thermofusible, telle que du polyéthylène, cette pièce formant manchon dans l'orifice 2 duquel viennent s'engager les extrémités, respectivement 3a, 4a de deux tubes 3, 4 cylindriques circulaires également en matière plastique thermofusible. Les tubes 3 et 4 sont disposés coaxialement, sensiblement dans l'axe 2a de l'orifice du manchon et ont un diamètre extérieur légèrement inférieur au diamètre ⌀ de l'orifice 2, de sorte que le manchon et les tubes présentent des surfaces correspondantes en vis-à-vis par lesquelles ils vont pouvoir être mutuellement reliés au cours du soudage.
- Pour la réunion des tubes, le manchon 1 comporte une résistnce électrique de chauffage 5 noyée dans son épaisseur, à proximité immédiate de sa surface intérieure repérée 1a.
- La résistance 5 est reliée par ses bornes 6a, 6b à une source d'énergie électrique (non représentée) propre à assurer une élévation suffisante de la température de la résistance pour induire le soudage des pièces entre elles.
- En l'espèce, la résistance 5 est constituée par un bobinage électrique cylindrique à section circulaire d'axe parallèle à celui du manchon et relié à la source électrique sus-mentionnée.
- Mais on aurait pu également envisager de noyer dans l'épaisseur du manchon une couche de matière présentant des qualités de conductivité électrique et de chauffage comparables à celles du bobinage.
- Pour le contrôle du soudage, la pièce de raccordement 1 est encore équipée de deux capteurs 7, 8 disposés dans des cavités 9, 10 dirigées chacune selon un axe 9a, 10a sensiblement radial à celui 2a des tubes, ces cavités s'étendant jusqu'au voisinage de la partie du bobinage en regard la plus voisine, en se terminant à un même niveau par une paroi de fond 11 que l'on distingue plus nettement sur les figures 2 à 4 (où l'on a représenté par souci de clarté des cavités sans capteur).
- Les capteurs 7, 8, en soi connus, peuvent par exemple consister en des micro-interrupteurs.
- Sur les dispositifs connus de ce type le processus de soudage des pièces est habituellement tel qu'une fois obtenu un chauffage suffisant de la résistance, la matière plastique qui l'environne entre en fusion et se dilate, induisant sous effet de cette pression de dilatation, une pénétration de matière ramollie dans le fond des cavités 9 et 10 puis, cette dilation se poursuivant, une remontée de matière dans les cavités jusqu'à ce que cette matière vienne exercer sur les capteurs 7 et 8 une action tendant à provoquer une interruption dans l'alimentation en énergie électrique de la résistance de chauffage, interrompant de ce fait le chauffage des pièces qu'on laisse alors refroidir.
- L'inconvénient d'un tel processus est que la pénétration de la matière ramollie ou fondue dans le fond de la cavité est induite sous l'action de la pression de dilatation de la matière, ce qui risque de conduire à un déclenchement trop rapide des capteurs et donc à une durée de chauffage des pièces insuffisante. Différentes mesures expérimentales ont en effet indiqué pour des jeux relativement faibles entre le diamètre intérieur du manchon (orifice 2) et le diamètre extérieur des tubes 3, 4, le temps de chauffage des pièces était insuffisant, la pression de dilation de la matière créant une remontée trop rapide de matière vers les capteurs.
- Pour éviter cet inconvénient, l'invention prévoit donc tout d'abord de disposer le fond 11 des cavités à une distance telle de la partie de la résistance de chauffage la plus proche que le fond 11 en question soit fondu sous l'effet du chauffage avant que la pression de dilatation soit suffisante pour pousser la matière fondue dans les cavités.
- Pour ce faire, il est nécessaire que h₁ soit inférieur ou égal à e avec :
h₁ : distance moyenne entre le fond 11 de chaque cavité et le plan général 15 tangent au bobinage et dans lequel s'étend la partie de la résistance qui est la plus voisine dudit fond, et
e : épaisseur de matière plastique constitutive du manchon 1 qui fond lors du chauffage des pièces. - En l'espèce, sur les figures 2 à 4, cette épaisseur e correspond à l'épaisseur de matière située, par rapport à l'axe du manchon, au-delà, ou à l'extérieur, du plan 15.
- Pour éviter par ailleurs qu'un écoulement trop rapide de matière ramollie dans la cavité conduise malgré tout à un arrêt prématuré du chauffage, l'invention prévoit en outre de contrôler la vitesse d'écoulement de la matière par une conformation rigoureuse des cavités de telle sorte que leur dimensionnement en section soit, au moins à proximité de leur fond et suivant un plan sensiblement perpendiculaire à leur axe (tel que 9a sur la figure 2), inférieur ou égal à l'épaisseur e précitée de matière ramollie.
- Ainsi, on va pouvoir assurer, quel que soit le jeu d'assemblage des pièces entre elles, tant une fusion du fond 11 des cavités avant que la pression de la matière ramollie soit suffisante pour le rompre, qu'un contrôle de la vitesse d'écoulement de cette même matière permettant de ne déclencher les capteurs 7 et 8 qu'à l'issue d'une durée de chauffage de la résistance 5 suffisante pour assurer, après refroidissement, une soudure de bonne qualité.
- Actuellement, la plupart, sinon la totalité, des capteurs 7, 8, existants sont installés à l'intérieur des cavités.
- Il pourra donc être utile dans certains cas, suivant la taille des capteurs utilisés, de disposer de cavités offrant un volume intérieur de réception relativement important.
- Aussi a-t-'on prévu la possibilité, telle qu'illustrée aux figures 3 et 4, de conformer ces cavités de telle sorte qu'elles élargissent comme on s'éloigne de leur paroi de fond 11, en présentant localement un épaulement périphérique 12.
- En pratique, ce brusque élargissement de section sera situé à une distance h₂ du plan général 15 défini ci-dessus telle que

- De cette façon, on disposera d'une hauteur de col

- Figure 3, on a par exemple illustrée une cavité se présentant sous l'aspect de deux cylindres accolés à section circulaire ayant successivement, en partant du fond 11, un diamètre d puis un diamètre D avec D > d.
- Dans ce cas, et en supposant que l'on utilise un manchon comportant un orifice 2 à section circulaire de diamètre ⌀, les conditions dimensionnelles à respecter pour obtenir un temps de chauffage des pièces assurant une soudure de bonne qualité seront :


d, h₁, et ⌀ étant exprimés en mm. - Et si l'on veut introduire comme paramètre l'épaisseur e définit ci-avant en tenant compte des résultats des essais qui ont été menés, les conditions dimensionnelles à respecter simultanément deviendront alors, en ce qui concerne la pièce de raccordement utilisée :

(d, h₂, h₁ et e étant toujours exprimés en mm). - Bien entendu, si la cavité était dépourvue d'épaulement, la condition portant sur h₂ n'aurait pas lieu d'être (cf. figure 2 où l'on a représenté une cavité 9 cyclindrique à section circulaire constante).
- Figure 4, on a représenté une autre variante de réalisation dans laquelle la cavité se présente sous la forme de deux cylindres à section circulaire de diamètre respectifs d et D réunis par un tronc de cône dont la petite base est située à la distance h₂ du plan 15 de la résistance 5.
- Il est clair que de nombreuses autres formes pourraient être envisagées pour les cavités, sous réserve que les caractéristiques dimensionnelles sus-mentionnées soient respectées le nombre de cavités et de capteurs étant fonction de l'application choisie.
- Egalement, l'invention est applicable à des pièces de raccordement autres que des manchons, telles par exemple que des prises de branchement ayant localement la forme d'une selle venant chevaucher la surface extérieure d'un tube pour son raccordement avec un autre tube disposé transversalement.
- Pour la clarté de la description sont présentés ci-après deux exemples d'essais qui ont été menés en vue du soudage d'un tube et d'un manchon comportant une cavité telle que celle illustrée figure 3 et un bobinage électrique pour le chauffage des pièces.


Claims (6)
- Dispositif pour détecter, au cours de son chauffage, des variations dans l'état physique d'une matière plastique thermofusible, ce dispositif comprenant :- une pièce (1) de raccordement prévue pour être soudée autour d'au moins une autre pièce (3, 4) tubulaire en matière plastique thermofusible, lesdites pièces présentant des surfaces respectivement intérieure (1a) et extérieure par lesquelles elles sont mutuellement reliées au cours du soudage, au moins une cavité (9, 10) au sein de laquelle la matière ramollie est susceptible de pénétrer étant ménagée dans ladite pièce de raccordement (1), cette cavité s'étendant suivant un axe sensiblement radial à la pièce tubulaire (3, 4) et à ladite pièce de raccordement, en se terminant par une paroi de fond (11) adjacente à ladite surface intérieure (1a) de la pièce de raccordement,- une résistance électrique (5) de chauffage noyée dans la pièce de raccordement (1) entre sadite surface intérieure (1a) et ladite cavité (9, 10), à une distance radiale minimum donnée h₁ de ladite paroi de fond (11) de la cavité, ladite résistance étant connectable à une source électrique pour faire fondre ladite matière thermofusible sur une épaisseur radiale prédéterminée de matière fondue en vue du soudage entre elles desdites pièces (1 ; 3, 4),- et au moins un capteur (7, 8) disposé dans ladite cavité (9, 10) pour y capter des variations d'état physique de la matière,
le dispositif étant caractérisé en ce que ladite distance radiale minimum donnée h₁ et le dimensionnement d en section, suivant un plan sensiblement perpendiculaire à son axe, de ladite cavité (9, 10) à proximité de sa paroi de fond (11), sont chacun sélectionnés pour être inférieurs ou égaux à l'épaisseur radiale prédéterminée de matière fondue e mesurée depuis ladite résistance (5) vers la surface extérieure de ladite pièce de raccordement. - Dispositif selon la revendication 1, caractérisé en ce que ladite distance radiale minimum h₁ a une valeur sensiblement égale à celle de l'épaisseur radiale prédéterminée de matière qui fond lors du chauffage desdites pièces (1 ; 3, 4) avant qu'une pression de dilatation induite par le chauffage provoque la pénétration de ladite matière fondue dans la cavité (9, 10) sur une épaisseur radiale e - h₁.
- Dispositif selon la revendication 1 ou la revendication 2, caractérisé en ce que la cavité (9 ) présente un épaulement (12) séparé de la résistance (5) d'une distance h₂ inférieure ou égale au double de ladite épaisseur radiale prédéterminée e de matière fondue, mesurée depuis la résistance (5) vers la surface extérieure de la pièce de raccordement (1).
- Dispositif selon l'une des revendications 1 à 3, caractérisé en ce que dans le cas où la pièce (1) de raccordement se présente sous la forme d'un manchon comportant un orifice (2) de section circulaire avec un diamètre (⌀), propre à recevoir intérieurement ladite pièce (3, 4) tubulaire, et où ladite cavité (9, 10) présente une section circulaire ou sensiblement circulaire, les relations suivantes sont vérifiées :


les valeurs de ⌀, d et h₁ étant exprimées en millimètre. - Dispositif selon la revendication 3, caractérisé en ce que dans le cas où la pièce (1) de raccordement se présente sous la forme d'un manchon comportant un orifice (2) à section circulaire de diamètre (⌀) propre à recevoir intérieurement au moins ladite pièce (3, 4) tubulaire, la relation suivante est vérifiée ;

Les valeurs de ⌀ et h₂ étant exprimées en millimètre. - Dispositif selon l'une quelconque des revendications 3 à 5, caractérisé en ce qu'il vérifie les relations suivantes :


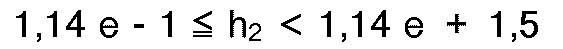


les valeurs de d, h₁, h₂, et e étant exprimées en millimètre.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR8817420 | 1988-12-29 | ||
| FR8817420A FR2643014B1 (fr) | 1988-12-29 | 1988-12-29 | Dispositif pour detecter, au cours du soudage, des variations dans l'etat physique de la matiere plastique d'une piece de raccordement prevue pour la jonction de tubes |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0376773A2 EP0376773A2 (fr) | 1990-07-04 |
| EP0376773A3 EP0376773A3 (fr) | 1991-09-18 |
| EP0376773B1 true EP0376773B1 (fr) | 1994-05-18 |
Family
ID=9373581
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19890403330 Expired - Lifetime EP0376773B1 (fr) | 1988-12-29 | 1989-11-30 | Dispositif pour détecter, au cours du soudage, des variations dans l'état physique de la matière plastique d'une pièce de raccordement prévue pour la jonction de tubes |
Country Status (13)
| Country | Link |
|---|---|
| US (1) | US5086213A (fr) |
| EP (1) | EP0376773B1 (fr) |
| JP (1) | JPH02270536A (fr) |
| KR (1) | KR0150425B1 (fr) |
| CN (1) | CN1027357C (fr) |
| AT (1) | ATE105769T1 (fr) |
| CA (1) | CA2004035C (fr) |
| DE (1) | DE68915420T2 (fr) |
| DZ (1) | DZ1376A1 (fr) |
| ES (1) | ES2048138T3 (fr) |
| FR (1) | FR2643014B1 (fr) |
| MC (1) | MC2067A1 (fr) |
| PT (1) | PT92749B (fr) |
Families Citing this family (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5252157A (en) * | 1989-05-01 | 1993-10-12 | Central Plastics Company | Electrothermal fusion of large diameter pipes by electric heating wire wrapping and sleeve connector |
| FR2648079B1 (fr) * | 1989-06-09 | 1991-11-15 | Boulet D Auria Teruzzi Cie | Procede de fabrication de manchon electro-soudable, dispositif pour la mise en oeuvre de celui-ci et manchons obtenus selon ce procede |
| US5369248A (en) * | 1992-09-01 | 1994-11-29 | Gaz De France | Electro-weldable connecting piece having connection terminals and its method of manufacture |
| DE29619326U1 (de) * | 1996-01-04 | 1997-02-20 | Geberit Technik Ag, Jona | Schweißmuffe |
| US5916468A (en) * | 1996-07-08 | 1999-06-29 | Hitachi Metals Ltd. | Electrically weldable pipe joint and production method thereof |
| US5770006A (en) * | 1997-01-13 | 1998-06-23 | Tdw Delaware, Inc. | Butt fusion machine for manufacturing full size segemented pipe turns |
| US5951902A (en) * | 1997-12-29 | 1999-09-14 | Kerotest Manufacturing Corp. | Method and apparatus for electrofusing thermoplastic |
| DE19807950A1 (de) * | 1998-02-25 | 1999-09-09 | Merle | Heizwendelfitting mit Schrumpfmantel |
| US6680464B1 (en) * | 2000-07-28 | 2004-01-20 | Zurn Industries, Inc. | Electrofusion joining control device |
| DE10328761B4 (de) | 2002-06-25 | 2005-06-23 | Friatec Ag | Schweißindikator für ein Schweißfitting |
| US20060202471A1 (en) * | 2005-03-07 | 2006-09-14 | Weisbond Bradley K | Electro-fusion joining system for thermoplastic piping systems |
| CN108621434A (zh) * | 2018-04-30 | 2018-10-09 | 上海英泰塑胶股份有限公司 | 连续纤维增强热塑性管道耐高压接口管件组及其制造方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| MC1581A1 (fr) * | 1983-12-02 | 1985-02-04 | Toutelectric | Procede pour le controle du temps de soudage |
| FR2555936B1 (fr) * | 1983-12-19 | 1986-11-21 | Toutelectric | Procede pour le controle du temps de soudage |
| AU581014B2 (en) * | 1984-08-28 | 1989-02-09 | Von Roll Ag | Weldable connecting member for connecting or joining thermoplastic pipe elements |
| GB8526235D0 (en) * | 1985-10-24 | 1985-11-27 | Glynwed Tubes & Fittings | Electrofusion coupler |
| CH672014A5 (fr) * | 1986-08-29 | 1989-10-13 | Fischer Ag Georg |
-
1988
- 1988-12-29 FR FR8817420A patent/FR2643014B1/fr not_active Expired - Lifetime
-
1989
- 1989-11-03 MC MC892080A patent/MC2067A1/fr unknown
- 1989-11-28 CA CA 2004035 patent/CA2004035C/fr not_active Expired - Lifetime
- 1989-11-30 DE DE68915420T patent/DE68915420T2/de not_active Expired - Lifetime
- 1989-11-30 AT AT89403330T patent/ATE105769T1/de not_active IP Right Cessation
- 1989-11-30 EP EP19890403330 patent/EP0376773B1/fr not_active Expired - Lifetime
- 1989-11-30 ES ES89403330T patent/ES2048138T3/es not_active Expired - Lifetime
- 1989-12-15 US US07/450,944 patent/US5086213A/en not_active Expired - Lifetime
- 1989-12-20 DZ DZ890189A patent/DZ1376A1/fr active
- 1989-12-28 CN CN89109752A patent/CN1027357C/zh not_active Expired - Lifetime
- 1989-12-28 PT PT92749A patent/PT92749B/pt not_active IP Right Cessation
- 1989-12-29 JP JP1344988A patent/JPH02270536A/ja active Pending
- 1989-12-29 KR KR1019890020127A patent/KR0150425B1/ko not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| PT92749B (pt) | 1996-01-31 |
| CA2004035A1 (fr) | 1990-06-29 |
| KR900009207A (ko) | 1990-07-02 |
| PT92749A (pt) | 1990-06-29 |
| US5086213A (en) | 1992-02-04 |
| EP0376773A3 (fr) | 1991-09-18 |
| CN1027357C (zh) | 1995-01-11 |
| EP0376773A2 (fr) | 1990-07-04 |
| DZ1376A1 (fr) | 2004-09-13 |
| FR2643014A1 (fr) | 1990-08-17 |
| MC2067A1 (fr) | 1990-10-03 |
| ES2048138T1 (es) | 1994-03-16 |
| ATE105769T1 (de) | 1994-06-15 |
| ES2048138T3 (es) | 1994-07-01 |
| CN1043659A (zh) | 1990-07-11 |
| DE68915420D1 (de) | 1994-06-23 |
| KR0150425B1 (ko) | 1998-11-16 |
| JPH02270536A (ja) | 1990-11-05 |
| CA2004035C (fr) | 2001-11-20 |
| DE68915420T2 (de) | 1994-09-01 |
| FR2643014B1 (fr) | 1991-05-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2031032C (fr) | Piece de raccordement du type a resistance electrique perfectionnee pour la reunion par thermosoudage d'elements en matiere plastique | |
| FR2654977A1 (fr) | Procede et piece de raccordement utilisant une resistance electrique pour le soudage d'elements en matiere plastique. | |
| CA2004035C (fr) | Dispositif pour detecter, au cours du soudage, des variations dans l'etat physique de la matiere plastique d'une piece de raccordement prevue pour la jonction de tubes | |
| MC1581A1 (fr) | Procede pour le controle du temps de soudage | |
| FR2497916A1 (fr) | Manchon soudable en matiere thermoplastique | |
| FR2913358A1 (fr) | Dispositif d'allumage d'une composition aluminothermique, creuset l'incorporant et procedes associes. | |
| CA1259367A (fr) | Dispositif de connexion electrique destine a etre place en paroi d'un four metallurgique a courant continu | |
| FR2692020A1 (fr) | Raccord thermosoudable pour tubes en un matériau plastique et son procédé de fabrication. | |
| FR2690036A1 (fr) | Filet formant résistance, son application au soudage de tubes aboutés et au raccordement transversal de canalisations, ensembles ainsi constitués et prise de branchement électrosoudable ainsi équipée. | |
| EP0145581A2 (fr) | Raccord de branchement en charge, résistance électrique pour un tel raccord et son procédé de fabrication | |
| EP0149410B1 (fr) | Procédé pour le contrôle du temps de soudage | |
| FR2588353A1 (fr) | Raccord notamment pour tubes et tuyaux | |
| FR2583948A1 (fr) | Resistance chauffante en feuille, bobine chauffante assemblee la comprenant et procede de fabrication de cette bobine | |
| FR2501104A1 (fr) | Procede et appareil pour souder des materiaux thermoplastiques | |
| FR2470367A1 (fr) | ||
| BE735915A (fr) | Tube muni d'un corps ä partir d'une feuille ou d'un tuyau et d'une tète, ainsi que procédé et dispositif pour la réalisation dudit tube | |
| EP0586283B1 (fr) | Pièce de raccordement électrosoudable à bornes de connexion perfectionnées et son procédé de fabrication | |
| FR2684062A1 (fr) | Fourche de bicyclette et procede de fabrication d'une telle fourche. | |
| BE1004518A5 (fr) | Detecteur pour fluides a haute temperature. | |
| EP0952240B1 (fr) | Dispositif de protection cathodique de cuve de chauffe-eau | |
| EP0105068A1 (fr) | Raccord électrosoudable en matière thermoplastique et procédé de fabrication | |
| EP0193425B1 (fr) | Procédé pour la fixation d'un tube mince entre une bague et un manchon tronconiques, et dispositifs pour la mise en oeuvre du procédé | |
| FR2535570A1 (fr) | Bande a chauffage electrique pour la realisation d'une jonction par manchon pour canalisation tubulaire thermiquement isolee, et son procede de fabrication | |
| FR2671159A1 (fr) | Perfectionnements a un systeme de canalisations et elements tubulaires adaptes. | |
| BE493962A (fr) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE ES GB GR IT LI LU NL SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE ES GB GR IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19911025 |
|
| 17Q | First examination report despatched |
Effective date: 19921102 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE ES GB GR IT LI LU NL SE |
|
| REF | Corresponds to: |
Ref document number: 105769 Country of ref document: AT Date of ref document: 19940615 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 68915420 Country of ref document: DE Date of ref document: 19940623 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2048138 Country of ref document: ES Kind code of ref document: T3 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19940607 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: FG4A Free format text: 3012798 |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 89403330.7 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20081029 Year of fee payment: 20 Ref country code: NL Payment date: 20081028 Year of fee payment: 20 Ref country code: DE Payment date: 20081126 Year of fee payment: 20 Ref country code: CH Payment date: 20081103 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20081023 Year of fee payment: 20 Ref country code: ES Payment date: 20081107 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20081031 Year of fee payment: 20 Ref country code: SE Payment date: 20081027 Year of fee payment: 20 Ref country code: IT Payment date: 20081117 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20081029 Year of fee payment: 20 Ref country code: GB Payment date: 20081029 Year of fee payment: 20 |
|
| BE20 | Be: patent expired |
Owner name: *GAZ DE FRANCE (SERVICE NATIONAL) Effective date: 20091130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20091129 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20091201 |
|
| NLV7 | Nl: ceased due to reaching the maximum lifetime of a patent |
Effective date: 20091130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20091130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20091129 Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20091201 |