EP0363667A2 - Continuous extruder for recovering the scraps originating from the machining of aluminum and its alloys, with production of extruded semifinished articles - Google Patents
Continuous extruder for recovering the scraps originating from the machining of aluminum and its alloys, with production of extruded semifinished articles Download PDFInfo
- Publication number
- EP0363667A2 EP0363667A2 EP89117010A EP89117010A EP0363667A2 EP 0363667 A2 EP0363667 A2 EP 0363667A2 EP 89117010 A EP89117010 A EP 89117010A EP 89117010 A EP89117010 A EP 89117010A EP 0363667 A2 EP0363667 A2 EP 0363667A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- scraps
- extruder
- ceramic material
- aluminum
- continuous
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C23/00—Extruding metal; Impact extrusion
- B21C23/005—Continuous extrusion starting from solid state material
Definitions
- the present invention relates to a continuous extruder for recovering the scraps, the swarf and the filings deriving from the machining of aluminum and its alloys, with continuous semifinished articles being produced, having the shape of rods, wires and bodies with various cross-section outlines.
- a purpose of the present invention is of providing a continuous extruder for recovering, as extruded semifinished articles, the scraps and the like, deriving from the machining of aluminum and of its alloys, which has such a structure as to directly accomplish the continuous extrusion at a high pressure and at a high temperature, with an useful life of the matrices and of the other parts subject to wear, which is considerably higher than of the extruders known from the prior art.
- Another purpose of the present invention is of providing a highly reliable extruder, such as to make it possible semifinished articles to be obtained which are endowed with improved surface qualities and with constant dimensional characteristics.
- a continuous extruder for recovering, as continuous-extruded semifinished articles, the scraps deriving from the machininig of aluminum and its alloys, and in particular scraps containing incorporated skins and oxides, suitable for being extruded under high specific pressures and at a high temperature
- extruder according to the present invention, the matrix and at least a portion of the tools comprising the inlet plates, the tight-sealing plate, the feed plate and the stop element, are made from a ceramic material selected from the group comprising the materials constituted by aluminum and silicon nitrides and oxides and the materials constituted by zirconium oxide, with said matrix and said tools of ceramic material being associated with an extruder having such a structure as to generate high specific pressures and a high temperature by internal friction, so as to make it possible said scraps to be extruded according to a direct, continuous extrusion method, with said scraps being transformed into semifinished
- said ceramic material is constituted by sintered or also electro-melted zirconium oxide, or by materials based on such compounds as Si3N4/Al2O3/SiO2/AlN variously combined with, and in different proportions to, one another, commonly denominated SIALON.
- a "Conform" extruder is substantially constituted by a revolving wheel 1, provided with a continuous peripheral, open groove 2.
- a portion, equivalent to about 1/4 of its length, of the groove 2 is tightly sealed by a stationary containment sole 3, which usually is constitued by a steel plate.
- An end of the sole 3 is into contact with a metal body 4 having an inner hollow, with whose upper end a matrix 5, also of steel, like the sole, is associated.
- the hollow 4a of the body 4 constitutes an expansion chamber which showed to be useful in order to extrude semifinished articles having a larger size than the materials fed to the extruder.
- the matrix 5 and the relevant expansion chamber are coaxial with each other and are positioned along a radial direction relatively to the wheel 1.
- a stop element 6 is positioned downstream the matrix 5 and is partially inserted inside the groove 2; its function is of diverting the material fed as a preformed rod 8, which advances between the sole and the groove, into the expansion chamber 4a and then into the matrix 5.
- the wear elements comprising a first inlet plate 9, a second inlet plate 10, a tight-sealing plate 11, a feed plate 4, the stop element 6 and the matrix 5, which are shaped according to the required type, shape and size of the desired extruded semifinished articles, are made from a SIALON ceramic material based on Si3N4/Al2O3/SiO2/AlN compounds.
- Said pre-treated scraps can be advantageously pre-compressed during the feed step, e.g., by means of an idling wheel, or any other equivalent means, not shown in the figure, and suitably positioned upstream the first inlet plate 8.
- the tools and the matrix are always kept into contact with each other and maintained in their position by means of a "block” or "sole” or “containment body” 12.
- the hollow element, or feed plate, 4 which constitutes the expansion chamber 4a and the stop element 6 are made from the same ceramic material which constitutes said inlet and sealing plates, and the matrix.
- the extruder provided according to the present invention showed to be particularly efficacious for recovering -- as a continuous-extruded rod -- scraps of aluminun and its alloys treated according to the recovery process as disclosed in the above cited patent application IT No. 19,813 A/86.
- the present Applicant was able to observe that the wear elements substantially constituted by the whole of the tools and matrix made from SIALON, extrusion ratios and speeds are achieved, which are higher than as obtainabke with the traditional extruders of "Conform" type.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacture And Refinement Of Metals (AREA)
Abstract
A continuous extruder for recovering, as continuous semifinished articles, the scraps deriving from the machininig of aluminum and its alloys, in which the matrix (5) and at least a portion of the tools comprising the inlet plates (9) and (10), the tight sealing plate (11), the feed plate (4) and the stop element (6) are made from a ceramic material selected from the group comprising the materials based on aluminum and silicon nitrides and oxides commonly denominated SIALON, and the materials based on zirconium oxide, with said matrix and said tools of ceramic material being associated with an extruder having such a structure as to generate high specific pressures and high temperatures by internal friction, so as to make it possible said semifinished articles to be extruded according to a direct, continuous extrusion method, with semifinished articles being produced.
Description
- The present invention relates to a continuous extruder for recovering the scraps, the swarf and the filings deriving from the machining of aluminum and its alloys, with continuous semifinished articles being produced, having the shape of rods, wires and bodies with various cross-section outlines.
- Those skilled in the art are aware of the fact that the recovery and re-use of the metal scraps are usually carried out by remelting them inside suitable furnaces, after submitting them to special treatments of washing, drying and compacting into block shapes, or the like. After being remelted, the liquid metal is cast and solidified, so as to capable of being extruded in order to yield shaped pieces. The technique of remelting with subsequent casting and extrusion involves in practice high investment costs, a high energy consumption and long processing times.
- In order to obviate these drawbacks, a recovery process was proposed in the past, in Italian patent application No. 19,813 A/86 (and corresponding European patent application No. 87102127.5) in the same Applicant's name, according to which the scraps from the machining of aluminum and its alloys, as off-cuts, swarf, filings and the like, containing incorporated oxides and "skins", are directly transformed into semifinished articles by means of a process of continuous extrusion under high specific pressures, comprised within the range of from 0.5x10⁶ kPa to 10⁶ kPa, and under such operating conditions that the temperature of the metal in the extrusion region is higher than 300°C.
- The extruders known from the prior art in order to accomplish these operating conditions, undergo in practice a rather fast wear, in particular due to the high temperatures reached in the friction and extrusion areas, and also due to the fact that the oxides and the skins contained in the scraps treated according to the above said process, directy submitted to extrusion, show a high abrasive power which reduces the useful life of all of those parts of the extruder which are most subject to wear.
- A purpose of the present invention is of providing a continuous extruder for recovering, as extruded semifinished articles, the scraps and the like, deriving from the machining of aluminum and of its alloys, which has such a structure as to directly accomplish the continuous extrusion at a high pressure and at a high temperature, with an useful life of the matrices and of the other parts subject to wear, which is considerably higher than of the extruders known from the prior art.
- Another purpose of the present invention is of providing a highly reliable extruder, such as to make it possible semifinished articles to be obtained which are endowed with improved surface qualities and with constant dimensional characteristics.
- These and still other purposes, which will be clearer from the following disclosure, are achieved by a continuous extruder for recovering, as continuous-extruded semifinished articles, the scraps deriving from the machininig of aluminum and its alloys, and in particular scraps containing incorporated skins and oxides, suitable for being extruded under high specific pressures and at a high temperature, in which extruder, according to the present invention, the matrix and at least a portion of the tools comprising the inlet plates, the tight-sealing plate, the feed plate and the stop element, are made from a ceramic material selected from the group comprising the materials constituted by aluminum and silicon nitrides and oxides and the materials constituted by zirconium oxide, with said matrix and said tools of ceramic material being associated with an extruder having such a structure as to generate high specific pressures and a high temperature by internal friction, so as to make it possible said scraps to be extruded according to a direct, continuous extrusion method, with said scraps being transformed into semifinished articles.
- More particularky, all of the parts of said extruder, which are most concerned by friction and wear during the extrusion under conditions of very high pressures and temperatures, are made from said ceramic material.
- More particularly, said ceramic material is constituted by sintered or also electro-melted zirconium oxide, or by materials based on such compounds as
Si₃N₄/Al₂O₃/SiO₂/AlN
variously combined with, and in different proportions to, one another, commonly denominated SIALON. - The present invention is now disclosed in greater detail according to a preferred, non-exclusive form of practical embodiment thereof, by referring to the hereto attached drawing table, given for merely indicative and non-limitative purposes, in which:
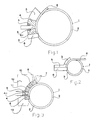
- Figure 1 shows a schematic view of a type of continuous extruder for accomplishing the well-known "Conform" (Trademark of UNITED KINGDOM ATOMIC ENERGY COMMISSION - GREAT BRITAIN) extrusion process;
- Figure 2 shows a differently structured form of the extruder of Figure 1, and
- Figure 3 shows a continuous extruder of "Conform" type structured according to the present invention.
- Referring to Figure 1, a "Conform" extruder is substantially constituted by a revolving wheel 1, provided with a continuous peripheral,
open groove 2. A portion, equivalent to about 1/4 of its length, of thegroove 2 is tightly sealed by astationary containment sole 3, which usually is constitued by a steel plate. An end of the sole 3 is into contact with ametal body 4 having an inner hollow, with whose upper end amatrix 5, also of steel, like the sole, is associated. The hollow 4a of thebody 4 constitutes an expansion chamber which showed to be useful in order to extrude semifinished articles having a larger size than the materials fed to the extruder. Thematrix 5 and the relevant expansion chamber are coaxial with each other and are positioned along a radial direction relatively to the wheel 1. Astop element 6 is positioned downstream thematrix 5 and is partially inserted inside thegroove 2; its function is of diverting the material fed as apreformed rod 8, which advances between the sole and the groove, into theexpansion chamber 4a and then into thematrix 5. - In Figure 2, on the contrary, the
stop element 6 is into contact with the hole of thematrix 5, so that theexpansion chamber 4a is no longer present. - In Figure 3, according to the technical solution proposed by the present invention, which showed to be particularly useful for accomplishing the direct extrusion of the scraps, the wear elements comprising a
first inlet plate 9, asecond inlet plate 10, a tight-sealing plate 11, afeed plate 4, thestop element 6 and thematrix 5, which are shaped according to the required type, shape and size of the desired extruded semifinished articles, are made from a SIALON ceramic material based on
Si₃N₄/Al₂O₃/SiO₂/AlN
compounds. - In this case (Figure 3), the scraps of aluminum and its alloys, already pre-treated according to as disclosed in above cited Italian patent application No. 19,813 A/86, and/or in corresponding European patent application 87102127.5, are fed into the groove of the wheel, at a point between the trail end of the
first inlet plate 9 and the same groove, by means of aloading hopper 7. - Said pre-treated scraps, still according to the present invention, can be advantageously pre-compressed during the feed step, e.g., by means of an idling wheel, or any other equivalent means, not shown in the figure, and suitably positioned upstream the
first inlet plate 8. - Still according to the present invention, the tools and the matrix are always kept into contact with each other and maintained in their position by means of a "block" or "sole" or "containment body" 12.
- Still according to the present invention, also the hollow element, or feed plate, 4, which constitutes the
expansion chamber 4a and thestop element 6 are made from the same ceramic material which constitutes said inlet and sealing plates, and the matrix. - The combination of the tools of ceramic material with a matrix also made from a ceramic material made it possible the useful life to be considerably increased of those parts which are most subject to wear during the extrusion, with the surface quality and the dimensional characteristics of the extruded semifinished articles being enhanced.
- In practice, the extruder provided according to the present invention showed to be particularly efficacious for recovering -- as a continuous-extruded rod -- scraps of aluminun and its alloys treated according to the recovery process as disclosed in the above cited patent application IT No. 19,813 A/86.
- Furthermore, on the basis of large-scale tests, the present Applicant was able to observe that the wear elements substantially constituted by the whole of the tools and matrix made from SIALON, extrusion ratios and speeds are achieved, which are higher than as obtainabke with the traditional extruders of "Conform" type.
- Finally, it is obvious that when the hereinabove finding is practiced, structurally equivalent modifications and variants may be supplied to it, without departing from the scope of protection of the same invention.
Claims (6)
1. Continuous extruder for recovering, as extruded semifinished articles, the scraps deriving from the machininig of aluminum and its alloys, in particular scraps containing incorporated skins and oxides, characterized in that the matrix and at least a portion of the tools comprising the inlet plates, the tight-sealing plate, the feed plate and the stop element are made from a ceramic material selected from the group comprising the materials constituted by aluminum and silicon nitrides and oxides and the materials constituted by zirconium oxide, with said matrix and said tools of ceramic material being associated with an extruder having such a structure as to generate high specific pressures and a high temperature by internal friction, so as to make it possible said scraps to be extruded according to a direct, continuous extrusion method, with said scraps being transformed into semifinished articles.
2. Continuous extruder according to claim 1 characterized in that all of its parts which are more subject to friction and wear during the extrusion, are made from a ceramic material.
3. Extruder according to claim 1 characterized in that said ceramic material is constituted by zirconium oxide, or by materials based on such compounds as
Si₃N₄/Al₂O₃/SiO₂/AlN
variously combined with, and in differnt proportions to, one another.
Si₃N₄/Al₂O₃/SiO₂/AlN
variously combined with, and in differnt proportions to, one another.
4. Extruder according to claim 1 characterized in that it is equipped with a hopper, or a suitable device for feeding said scraps to be extruded.
5. Extruder according to claim 1 characterized in that said scraps are pre-compressed during their feeding step by means of an idling wheel, or of an equivalent device known from the prior art.
6. Extruder according to the preceding claims, characterized in that it is provided for such purposes and uses as hereinabove specified according to as disclosed and illustrated.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT2226888 | 1988-10-11 | ||
| IT8822268A IT1230511B (en) | 1988-10-11 | 1988-10-11 | CONTINUOUS EXTRUDER FOR THE RECOVERY OF WASTE FROM MECHANICAL ALUMINUM PROCESSING AND ITS ALLOYS WITH PRODUCTION OF EXTRUDED SEMI-FINISHED PRODUCTS |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0363667A2 true EP0363667A2 (en) | 1990-04-18 |
| EP0363667A3 EP0363667A3 (en) | 1991-01-02 |
Family
ID=11193917
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19890117010 Withdrawn EP0363667A3 (en) | 1988-10-11 | 1989-09-14 | Continuous extruder for recovering the scraps originating from the machining of aluminum and its alloys, with production of extruded semifinished articles |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0363667A3 (en) |
| IT (1) | IT1230511B (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5595084A (en) * | 1994-04-12 | 1997-01-21 | Yugen Kaisha Yano Engineering | Hollow die and an apparatus for continuous extrusion forming of hollow articles |
| CN100409958C (en) * | 2006-09-29 | 2008-08-13 | 大连康丰科技有限公司 | A chamber of a combined continuous extrusion machine |
| CN104043669A (en) * | 2013-03-15 | 2014-09-17 | 南线有限责任公司 | Providing plastic zone extrusion |
| CN105817490A (en) * | 2015-05-27 | 2016-08-03 | 河南华洋铜业集团有限公司 | Aluminum extrusion device and its extruding cavity structure |
| US9616497B2 (en) | 2010-07-09 | 2017-04-11 | Southwire Company | Providing plastic zone extrusion |
-
1988
- 1988-10-11 IT IT8822268A patent/IT1230511B/en active
-
1989
- 1989-09-14 EP EP19890117010 patent/EP0363667A3/en not_active Withdrawn
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5595084A (en) * | 1994-04-12 | 1997-01-21 | Yugen Kaisha Yano Engineering | Hollow die and an apparatus for continuous extrusion forming of hollow articles |
| CN100409958C (en) * | 2006-09-29 | 2008-08-13 | 大连康丰科技有限公司 | A chamber of a combined continuous extrusion machine |
| US9616497B2 (en) | 2010-07-09 | 2017-04-11 | Southwire Company | Providing plastic zone extrusion |
| CN104043669A (en) * | 2013-03-15 | 2014-09-17 | 南线有限责任公司 | Providing plastic zone extrusion |
| EP2777837A1 (en) * | 2013-03-15 | 2014-09-17 | Southwire Company, LLC | System for and method of plastic zone extrusion |
| CN105817490A (en) * | 2015-05-27 | 2016-08-03 | 河南华洋铜业集团有限公司 | Aluminum extrusion device and its extruding cavity structure |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0363667A3 (en) | 1991-01-02 |
| IT1230511B (en) | 1991-10-25 |
| IT8822268A0 (en) | 1988-10-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| FR2671992B1 (en) | COLD CHAMBER PRESSURE CASTING PROCESS. | |
| CA2000776A1 (en) | A flotation process for the formation of metal matrix composite bodies | |
| US5230382A (en) | Process of producing individual eccentric cams from cast metal | |
| EP0363667A3 (en) | Continuous extruder for recovering the scraps originating from the machining of aluminum and its alloys, with production of extruded semifinished articles | |
| EP0241668A1 (en) | Process for recovering the scraps deriving from the machining of aluminum and its alloys,with production of extruded semifinished articles | |
| Dower et al. | The utilization of mild steel machining swarf in hot forging | |
| JPS5758947A (en) | Cold pressing method for cold pressed parts such as bolt or the like | |
| Baranchikov et al. | Developments in Technology of Rolling Annular Semi-Products From Aluminium Alloys | |
| JPS5441232A (en) | Metallic material covering method | |
| SU1285025A1 (en) | Method of manufacturing nipples of heating radiators from malleable cast iron | |
| Sheng | Forging of 4 Cr 5 MoSiV 1 die steel | |
| SU1026965A1 (en) | Method of producing bimetallic cutting tool | |
| SU965584A1 (en) | Blanking die cutting portion producing method | |
| SU1648584A1 (en) | Method for pressing materials without butt | |
| Polek et al. | The Technology of Hot Extrusion Processes for Steel Tubes | |
| Li et al. | The Development of a Novel B--Ti--RE Modified H 13 Cast Dies for Aluminium Alloy | |
| JPS5588966A (en) | Injection pump of hot chamber type die casting machine | |
| SU662212A1 (en) | Combination die set | |
| SU1748908A1 (en) | Method of manufacturing encompassing and encompassed die parts | |
| SU1479245A1 (en) | Method of diffusion vacuum welding | |
| SU1734954A1 (en) | Method of making bimetallic workpieces from high-speed steel powder | |
| DE2346586A1 (en) | Cutting edges produced by hot-pressing silicon nitride powder - for turning light metal articles, esp. aluminium pistons | |
| Sabath | EM Casting of Aluminum Alloys.(WAA Translation Available) | |
| Lazorkin | Resource-saving technological processes of metal-ware production | |
| Kornilov et al. | Development of rolling-pressing for manufacturing the profiles, tubes and wire fabricated from nonferrous metals and alloys |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE ES FR GB GR LI LU NL SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE ES FR GB GR LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19910615 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19930401 |