EP0062524B1 - Improved casting apparatus - Google Patents
Improved casting apparatus Download PDFInfo
- Publication number
- EP0062524B1 EP0062524B1 EP82301782A EP82301782A EP0062524B1 EP 0062524 B1 EP0062524 B1 EP 0062524B1 EP 82301782 A EP82301782 A EP 82301782A EP 82301782 A EP82301782 A EP 82301782A EP 0062524 B1 EP0062524 B1 EP 0062524B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheath
- lengths
- refractory
- box
- junction box
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 238000005266 casting Methods 0.000 title description 7
- 239000002184 metal Substances 0.000 claims abstract description 21
- 239000011236 particulate material Substances 0.000 claims abstract description 7
- 239000011111 cardboard Substances 0.000 claims abstract description 4
- 239000011819 refractory material Substances 0.000 claims description 4
- 239000000123 paper Substances 0.000 claims description 2
- 230000000295 complement effect Effects 0.000 claims 1
- 239000004576 sand Substances 0.000 abstract description 16
- 238000000034 method Methods 0.000 description 4
- 229910000831 Steel Inorganic materials 0.000 description 2
- 230000003628 erosive effect Effects 0.000 description 2
- 239000003292 glue Substances 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 239000010959 steel Substances 0.000 description 2
- 230000008901 benefit Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000001627 detrimental effect Effects 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000005058 metal casting Methods 0.000 description 1
- 239000011087 paperboard Substances 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D35/00—Equipment for conveying molten metal into beds or moulds
- B22D35/04—Equipment for conveying molten metal into beds or moulds into moulds, e.g. base plates, runners
Definitions
- This invention relates to the casting of molten metal and is particularly concerned with improved apparatus for supplying molten metal to a metallurgical mould,
- Refractory gating systems for casting moulds are built by abutting a number of separate, standard proprietary pieces know collectively as "refractory holloware", to form conduits or channels which conduct molten metal from the pouring ladle or tundish into the mould cavity.
- the most common piece of refractory holloware in refractory gating systems is a short length of cylindrical piping having a nominal inner diameter and a nominal larger outer diameter. Longer lengths are made by assembling these lengths end to end to produce for example, horizontal and vertical channels.
- junction boxes are used which have facilities for connecting two or more pipes mutually perpendicular to each other.
- the gating system assembly is normally held in position by a particulate material e.g. sand, which is rammed up around and against the outer surface of the system. It is also known to supply molten metal via pouring trumpets leading to moulds for bulk steel such as ingot moulds.
- the refractory holloware is usually made from a fired fireclay or the like and it is recognised that these materials tend to shrink when cast in moulds.
- the industry standards will accept a ⁇ 1.5% variation in diameter from the nominal value - see British Standard BS 2496:1968. The variation in tolerances aggravates the risk that adjacent lengths of pipe may not fit accurately together, and there will be gaps. It is known to provide the individual pipe lengths with a male and female spigot joint which is an improvement but the spigot joints do not form a tight fit and there are still often gaps between joints through which sand can penetrate. Also, in certain foundries there are large numbers of patterns with a small number of moulds made from each pattern and this precludes the use of standard length refractory pipes.
- BE-A-886139 discloses a transfer system for supplying molten metal from a vessel via a runner to a series of ingot moulds.
- the runner comprises a conduit built up of plurality of lengths of refractory pipe joined in end-to-end relation, the lengths being enclosed by an outer sheath in the form of a refractory tube, the annular clearance between the pipes and the refractory tube being filled with set refractory material.
- the end of the refractory tube is stood on a distribution box.
- DE-C-529889 discloses a runner system comprising a set of inner and outer tubes, these being formed of the same material and length. The inner tubes are received as a tight fit within the outer tubes so that molten metal within the inner tube is prevented from reaching sand in which the runner system is embedded.
- mould apparatus comprising a mould box containing a pattern in the shape of an article to be cast of molten metal, a gating system connected to a pattern and comprising a conduit formed of lengths of refractory pipe joined in end-to-end relation, whereby these lengths of refractory pipe are enclosed in an outer sheath characterised in that the gating system includes at least one junction box where the conduit changes direction, and in that the junction box has extension pieces, each extension piece projecting away from a wall of the junction box and reducing in its outer diameter, and in that the outer sheath is sealed at its ends to the extension pieces of the boxes.
- the outer sheath is relatively much longer than any one length of refractory pipe or extension piece so that a joint of the sheath with the junction box is longitudinally spaced from a joint of the refractory pipe by a sufficient distance to define a tortuous path to the ingress of particulate material. In this way if particulate material enters a joint in the sheath it will not readily be able to travel sufficient distance to a joint of the refractory pipes to penetrate through and foul the conduit.
- the sheath is a tubular element adapted to engage the junction box extension piece at each end. It is not however necessary that the sheath be of substantially constant shape and configuration along its length.
- the sheath may have a longitudinal cut or seam, the edges of which may be urged together to form a fluid tight seal and held in that condition e.g. by a tape.
- the sheath comprises one or more close fitting carboard paper or metal tubes, the inner diameter of which is selected to be slightly greater than the nominal outer diameter or the refractory pieces. Whereas the lengths of holloware cannot be made to close tolerances, such tubes can be made to very close tolerances. Tubes of paper or cardboard are preferred for economy and lightness of weight while metal tubes are more reusable.
- the sheath allows simple alignment of the various refractory pieces since they can be loaded one at a time into the tubes and this eliminates any reduction in cross sectional area of the gating system due to misalignment. It also eliminates the need for spigot joints on all the refractory pieces thereby reducing the cost of these refractory pieces.
- the relative dimensions of the sheath and the pipes are chosen such that the sheaths are sufficiently tight-fitting to enable pre-assembly of part or all of the gating system to form a freestanding rigid unit. This can then be lifted and transported as one unit, so simplifying movement, positioning and alignment of the pre-assembled parts and reducing the assembly time.
- the assembled unit is then placed in a mould box and connected to the pattern and particulate material e.g. a foundry sand, is then rammed around the pattern and its conduits.
- the invention may be applied to a variety of techniques involving the casting of metal shapes in mould boxes.
- the invention is ideally suited to the so-called "V" process, especially for larger moulds.
- the gating system is incorporated in the lower ("drag") half of the mould box and not on the parting line. Gating from below is preferred since this results in much better metal flow characteristics.
- a junction box is necessary to accommodate changes in direction in the refractory holloware and to present a highly erosion resistant refractory surface on to which molten metal may fall.
- the invention also includes for use with apparatus a junction box formed of refractory material and having a passageway with at least one inlet and at least one outlet and including an angled portion, an extension piece is present about the outlet of each bore and projects from a wall of the box and reduces the external diameter away from the wall.
- the junction box may have any required combination of inlet and outlets and may be of various shapes e.g. like the letters "L”, “T”, "X” and "Y”.
- the mould box of Figure 1 comprises two halves 1, 2 the lower 1 being the drag half and the upper being the cope half.
- a mould pattern 3 is present in the box and below this is located a gating system G. Molten metal is fed into the gating system G via a downrunner A.
- the mould and the gating system are supported in compacted foundry sand 4 which extends almost to the top of the box.
- the gating system is built up of a number of lengths of refractory pipe P.
- Each pipe is cast of a refractory material e.g. a fired fireclay and has flat end walls whereby adjacent lengths may be abutted together.
- the pipe lengths are about 30 cm long and can be moulded to a nominal external diameter of about 147 mm. In practice the diameter will vary within a tolerance of about ⁇ 1.5%.
- the lengths of pipe P are received in a sheath S, preferably a carboard sheath being a factory made item; for a pipe having a nominal external diameter of 147 mm, the sheath S should have an internal diameter of 150 mm.
- the wall thickness may be about 4mm and the cardboard may be fireproofed.
- the sheath S is fitted over one or more lengths of pipe P.
- the sheath may extend over them all or may be cut to size; Exposed ends of sheath S may be sealed to the pipe P using tape T or the like.
- the pipe lengths are received in the sheath, then depending on the variation of tolerance they may be a relatively tight fit or there may be an annular gap of from say 0.5 mm to 2.5 mm: despite this they are held in the sheath which thus is a selfsupporting unit for transport.
- the gating system G thus comprises a conduit of constant internal diameter, which is sand tight despite being surrounded by compacted foundry sand.
- junction box J of the invention comprises a body 5 moulded of refractory fireclay.
- the box has a through bore 6 having one or more inlet and outlets.
- the mouth of each bore end is surrounded by an extension piece E which is integrally moulded with the body.
- the extension piece measures about 50 mm in length and has a bore extension 7 which is the same as that of the bore 6.
- the external diameter of the extension piece at its root to the junction box body 5 is about 150 mm and the extension piece tapers towards its free end 4 to an external diameter of about 147 mm. (These are nominal dimensions and in accordance with conventional practice they may vary within a tolerance of about ⁇ 1.5%.)
- One end of the sheath S is forced over the extension piece E of one junction box and then over the other so forming a sealed system.
- the extension piece of junction box J1 is below nominal; the vertical sheath S and the horizontal sheath S thus fit over the extension and abut the wall.
- the extension piece exceeds nominal external diameter and so the vertical sheath S and the horizontal sheath S only engages a sloping portion thereof.
- the mould box was used to cast an article of a defined shape.
Landscapes
- Mechanical Engineering (AREA)
- Engineering & Computer Science (AREA)
- Confectionery (AREA)
- Furnace Housings, Linings, Walls, And Ceilings (AREA)
- Processing Of Solid Wastes (AREA)
- Treatment Of Steel In Its Molten State (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
- Automatic Cycles, And Cycles In General (AREA)
- Connection Or Junction Boxes (AREA)
- Manufacture Of Alloys Or Alloy Compounds (AREA)
- Body Structure For Vehicles (AREA)
- Pretreatment Of Seeds And Plants (AREA)
- Other Liquid Machine Or Engine Such As Wave Power Use (AREA)
Abstract
Description
- This invention relates to the casting of molten metal and is particularly concerned with improved apparatus for supplying molten metal to a metallurgical mould,
- Refractory gating systems for casting moulds are built by abutting a number of separate, standard proprietary pieces know collectively as "refractory holloware", to form conduits or channels which conduct molten metal from the pouring ladle or tundish into the mould cavity. The most common piece of refractory holloware in refractory gating systems is a short length of cylindrical piping having a nominal inner diameter and a nominal larger outer diameter. Longer lengths are made by assembling these lengths end to end to produce for example, horizontal and vertical channels. To conduct the molten metal around bends, junction boxes are used which have facilities for connecting two or more pipes mutually perpendicular to each other. The gating system assembly is normally held in position by a particulate material e.g. sand, which is rammed up around and against the outer surface of the system. It is also known to supply molten metal via pouring trumpets leading to moulds for bulk steel such as ingot moulds.
- There is no simple method for aligning the various pieces of refractory holloware and for sealing the joints such that sand cannot enter the gating system or remain trapped between the joints and be subsequently carried into the mould cavity by the flowing steel. If sand is carried into the mould cavity, there will be inclusions in the casting which can be very expensive to remove and can even lead to the casting being scrapped.
- The refractory holloware is usually made from a fired fireclay or the like and it is recognised that these materials tend to shrink when cast in moulds. The industry standards will accept a ±1.5% variation in diameter from the nominal value - see British Standard BS 2496:1968. The variation in tolerances aggravates the risk that adjacent lengths of pipe may not fit accurately together, and there will be gaps. It is known to provide the individual pipe lengths with a male and female spigot joint which is an improvement but the spigot joints do not form a tight fit and there are still often gaps between joints through which sand can penetrate. Also, in certain foundries there are large numbers of patterns with a small number of moulds made from each pattern and this precludes the use of standard length refractory pipes. The standard lengths are often cut to size on site and the benefit of having refractory holloware formed complete with spigot joints is lost. Severe misalignment between the refractory pieces often occurs reducing the cross- sectional area of the gating system at these points which results in low pouring rates and throttled ladle stream which can reduce casting quality.
- It is also known to tape or glue refractory pieces together. These methods are slow and require much skill and care to ensure that the pieces are correctly aligned and the joints are sealed tight. Furthermore, when the molten metal contacts any glue used in aligning the gating system, a vigorous reaction can occur, leading to turbulent metal flow and gas defects within the metal, both of which are detrimental to casting quality.
- BE-A-886139 discloses a transfer system for supplying molten metal from a vessel via a runner to a series of ingot moulds. The runner comprises a conduit built up of plurality of lengths of refractory pipe joined in end-to-end relation, the lengths being enclosed by an outer sheath in the form of a refractory tube, the annular clearance between the pipes and the refractory tube being filled with set refractory material. The end of the refractory tube is stood on a distribution box. DE-C-529889 discloses a runner system comprising a set of inner and outer tubes, these being formed of the same material and length. The inner tubes are received as a tight fit within the outer tubes so that molten metal within the inner tube is prevented from reaching sand in which the runner system is embedded.
- One object of the invention is to provide apparatus which can, in a rapid and simple manner, allow the improved alignment of separate pieces of refractory holloware. Another object of the invention is to prevent sand entering the gating system through gaps at the positions where the pieces are joined together.
- According to one aspect of this invention there is provided mould apparatus comprising a mould box containing a pattern in the shape of an article to be cast of molten metal, a gating system connected to a pattern and comprising a conduit formed of lengths of refractory pipe joined in end-to-end relation, whereby these lengths of refractory pipe are enclosed in an outer sheath characterised in that the gating system includes at least one junction box where the conduit changes direction, and in that the junction box has extension pieces, each extension piece projecting away from a wall of the junction box and reducing in its outer diameter, and in that the outer sheath is sealed at its ends to the extension pieces of the boxes.
- Most preferably the outer sheath is relatively much longer than any one length of refractory pipe or extension piece so that a joint of the sheath with the junction box is longitudinally spaced from a joint of the refractory pipe by a sufficient distance to define a tortuous path to the ingress of particulate material. In this way if particulate material enters a joint in the sheath it will not readily be able to travel sufficient distance to a joint of the refractory pipes to penetrate through and foul the conduit.
- The sheath is a tubular element adapted to engage the junction box extension piece at each end. It is not however necessary that the sheath be of substantially constant shape and configuration along its length. For example, the sheath may have a longitudinal cut or seam, the edges of which may be urged together to form a fluid tight seal and held in that condition e.g. by a tape.
- Preferably the sheath comprises one or more close fitting carboard paper or metal tubes, the inner diameter of which is selected to be slightly greater than the nominal outer diameter or the refractory pieces. Whereas the lengths of holloware cannot be made to close tolerances, such tubes can be made to very close tolerances. Tubes of paper or cardboard are preferred for economy and lightness of weight while metal tubes are more reusable. The sheath allows simple alignment of the various refractory pieces since they can be loaded one at a time into the tubes and this eliminates any reduction in cross sectional area of the gating system due to misalignment. It also eliminates the need for spigot joints on all the refractory pieces thereby reducing the cost of these refractory pieces.
- In a much preferred embodiment of the invention the relative dimensions of the sheath and the pipes are chosen such that the sheaths are sufficiently tight-fitting to enable pre-assembly of part or all of the gating system to form a freestanding rigid unit. This can then be lifted and transported as one unit, so simplifying movement, positioning and alignment of the pre-assembled parts and reducing the assembly time. The assembled unit is then placed in a mould box and connected to the pattern and particulate material e.g. a foundry sand, is then rammed around the pattern and its conduits.
- The invention may be applied to a variety of techniques involving the casting of metal shapes in mould boxes. The invention is ideally suited to the so-called "V" process, especially for larger moulds. In such a case the gating system is incorporated in the lower ("drag") half of the mould box and not on the parting line. Gating from below is preferred since this results in much better metal flow characteristics. After forming the plastics sheet over the drag pattern and with the box in position the gating system is assembled and the ends of the sheath are sealed to the sheet with e.g. tape. Loose sand is then fed in and the mould box vibrated; the system is sufficiently self supporting and said tight not to be affected by the vibration. The mould is completed as usual and in this way is provided with a vacuum tight and erosion resistant gating system providing optimum flow characteristics of metal into mould.
- A junction box is necessary to accommodate changes in direction in the refractory holloware and to present a highly erosion resistant refractory surface on to which molten metal may fall.
- The invention also includes for use with apparatus a junction box formed of refractory material and having a passageway with at least one inlet and at least one outlet and including an angled portion, an extension piece is present about the outlet of each bore and projects from a wall of the box and reduces the external diameter away from the wall. The junction box may have any required combination of inlet and outlets and may be of various shapes e.g. like the letters "L", "T", "X" and "Y".
- In order that the invention may be well understood it will now be described by way of example with reference to the accompanying diagrammatic drawings, in which
- Figure 1 is a view of a mould box a wall of which has been removed to show the interior;
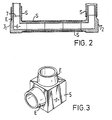
- Figure 2 is a sectional view of part of the gating system;
- Figure 3 is a perspective view of a junction box drawn to a much enlarged scale.
- The mould box of Figure 1 comprises two
halves 1, 2 the lower 1 being the drag half and the upper being the cope half. A mould pattern 3 is present in the box and below this is located a gating system G. Molten metal is fed into the gating system G via a downrunner A. The mould and the gating system are supported in compacted foundry sand 4 which extends almost to the top of the box. - The gating system is built up of a number of lengths of refractory pipe P. Each pipe is cast of a refractory material e.g. a fired fireclay and has flat end walls whereby adjacent lengths may be abutted together. The pipe lengths are about 30 cm long and can be moulded to a nominal external diameter of about 147 mm. In practice the diameter will vary within a tolerance of about ±1.5%. According to the invention, the lengths of pipe P are received in a sheath S, preferably a carboard sheath being a factory made item; for a pipe having a nominal external diameter of 147 mm, the sheath S should have an internal diameter of 150 mm. The wall thickness may be about 4mm and the cardboard may be fireproofed.
- In use, the sheath S is fitted over one or more lengths of pipe P. Depending on the length of pipe and the number of pipes the sheath may extend over them all or may be cut to size; Exposed ends of sheath S may be sealed to the pipe P using tape T or the like. When the pipe lengths are received in the sheath, then depending on the variation of tolerance they may be a relatively tight fit or there may be an annular gap of from say 0.5 mm to 2.5 mm: despite this they are held in the sheath which thus is a selfsupporting unit for transport. Because there is a substantial longitudinal distance from one end of the sheath to a joint between two abutting lengths of pipe, there is no, risk that sand 4 will enter the sheath S and pass through the joint into the metal stream. Even if the sand enters the gap between the sheath and the joint it must travel a tortuous path, changing direction through a right angle and it is most unlikely that sand could travel in this way. The gating system G thus comprises a conduit of constant internal diameter, which is sand tight despite being surrounded by compacted foundry sand.
- Where the gating system has a change of direction e.g. a corner unit or a T joint, use is made of a junction box J of the invention. The junction box comprises a
body 5 moulded of refractory fireclay. The box has a through bore 6 having one or more inlet and outlets. The mouth of each bore end is surrounded by an extension piece E which is integrally moulded with the body. The extension piece measures about 50 mm in length and has abore extension 7 which is the same as that of the bore 6. The external diameter of the extension piece at its root to thejunction box body 5 is about 150 mm and the extension piece tapers towards its free end 4 to an external diameter of about 147 mm. (These are nominal dimensions and in accordance with conventional practice they may vary within a tolerance of about ±1.5%.) - One end of the sheath S is forced over the extension piece E of one junction box and then over the other so forming a sealed system. Despite the fact that parts are not made to close tolerances, the system is nonetheless sealed. For example and as shown in Figure 2, the extension piece of junction box J1 is below nominal; the vertical sheath S and the horizontal sheath S thus fit over the extension and abut the wall. In the case of junction box J2, the extension piece exceeds nominal external diameter and so the vertical sheath S and the horizontal sheath S only engages a sloping portion thereof.
- In the foregoing description the mould box was used to cast an article of a defined shape.
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT82301782T ATE14394T1 (en) | 1981-04-04 | 1982-04-05 | CASTING DEVICE. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| GB8110605 | 1981-04-04 | ||
| GB8110605 | 1981-04-04 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0062524A2 EP0062524A2 (en) | 1982-10-13 |
| EP0062524A3 EP0062524A3 (en) | 1982-12-08 |
| EP0062524B1 true EP0062524B1 (en) | 1985-07-24 |
Family
ID=10520932
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP82301782A Expired EP0062524B1 (en) | 1981-04-04 | 1982-04-05 | Improved casting apparatus |
Country Status (9)
| Country | Link |
|---|---|
| EP (1) | EP0062524B1 (en) |
| JP (1) | JPS57184554A (en) |
| AT (1) | ATE14394T1 (en) |
| AU (1) | AU543890B2 (en) |
| BR (1) | BR8201992A (en) |
| CA (1) | CA1185764A (en) |
| DE (1) | DE3264858D1 (en) |
| ES (2) | ES511090A0 (en) |
| ZA (1) | ZA822137B (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4506813A (en) * | 1979-12-15 | 1985-03-26 | Dughan Terence G | Tubular assembly, method of preparing the assembly, apparatus for uphill teeming which incorporates the assembly and method of casting metal |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1199443B (en) * | 1961-01-31 | 1965-08-26 | Borsig Ag | Protective cladding for the pouring system of castings, especially of cast steel |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE529899C (en) * | 1930-03-08 | 1931-07-18 | Werner Studte | Sewer stone made for itself made of casing and core pipe |
| AU6403380A (en) * | 1979-11-14 | 1981-05-21 | Dyson Refractories Ltd. | Casting of molten metal |
-
1982
- 1982-03-29 ZA ZA822137A patent/ZA822137B/en unknown
- 1982-03-31 AU AU82196/82A patent/AU543890B2/en not_active Ceased
- 1982-03-31 CA CA000400254A patent/CA1185764A/en not_active Expired
- 1982-04-02 JP JP57055258A patent/JPS57184554A/en active Pending
- 1982-04-02 ES ES511090A patent/ES511090A0/en active Granted
- 1982-04-05 EP EP82301782A patent/EP0062524B1/en not_active Expired
- 1982-04-05 BR BR8201992A patent/BR8201992A/en unknown
- 1982-04-05 DE DE8282301782T patent/DE3264858D1/en not_active Expired
- 1982-04-05 AT AT82301782T patent/ATE14394T1/en active
-
1983
- 1983-04-15 ES ES521504A patent/ES521504A0/en active Granted
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1199443B (en) * | 1961-01-31 | 1965-08-26 | Borsig Ag | Protective cladding for the pouring system of castings, especially of cast steel |
Also Published As
| Publication number | Publication date |
|---|---|
| ES8307137A1 (en) | 1983-07-01 |
| AU8219682A (en) | 1982-10-14 |
| ZA822137B (en) | 1983-03-30 |
| EP0062524A2 (en) | 1982-10-13 |
| CA1185764A (en) | 1985-04-23 |
| AU543890B2 (en) | 1985-05-09 |
| ATE14394T1 (en) | 1985-08-15 |
| ES8404890A1 (en) | 1984-05-16 |
| BR8201992A (en) | 1983-03-15 |
| EP0062524A3 (en) | 1982-12-08 |
| DE3264858D1 (en) | 1985-08-29 |
| ES511090A0 (en) | 1983-07-01 |
| JPS57184554A (en) | 1982-11-13 |
| ES521504A0 (en) | 1984-05-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5402993A (en) | Immersion casting pipe for thin slabs | |
| EP0572058B1 (en) | Mould for producing thin-wall castings by gravity pouring | |
| ES8307146A1 (en) | Metal pouring nozzle with gas inlet | |
| CA1185764A (en) | Casting apparatus and method | |
| GB8604385D0 (en) | Casting | |
| GB2111880A (en) | Immersion pouring spout for continuous casting | |
| CA1243188A (en) | Submerged nozzle for use in the continuous casting of slabs | |
| US5118016A (en) | Bottom pour tiles with self sealing joint for pouring liquid steel | |
| US4913403A (en) | Runner system and article for the casting of metals | |
| US5158217A (en) | Twist lock junction between refractory tubular shapes | |
| EP0073573A1 (en) | Controlled transfer of molten metal | |
| EP0313052B1 (en) | Tundish for horizontal continuous casting | |
| SU997970A1 (en) | Unit for low pressure die casting of multilayer metallic blanks | |
| WO1997004901A1 (en) | Limiting ingress of gas to continuous caster | |
| EP0563376B1 (en) | Gaz blowing plate brick or nozzle brick for molten metal | |
| SU1061916A1 (en) | Apparatus for preventing secondary oxidation of metal in continuous casting | |
| US6412672B1 (en) | Ladle to tundish transfer to molten metal in the steelmaking process | |
| Smith | Method of and Apparatus for Casting | |
| Lee et al. | Welded Aluminum Die Cast Article | |
| Hofmann et al. | Immersion casting pipe for thin slabs | |
| Schneider et al. | Gas and parting-agent conduit and distribution system for a continuous casting plant | |
| JPS5772762A (en) | Casting mold | |
| JPS61195753A (en) | Continuous casting equipment | |
| Dechant et al. | Trend-Setting New Processing Line in a Foundry for Light Metal Sand Castings | |
| Iida | Automation in Continuous Casting Process |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH DE FR GB IT NL SE |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH DE FR GB IT NL SE |
|
| 17P | Request for examination filed |
Effective date: 19830607 |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH DE FR GB IT LI NL SE |
|
| REF | Corresponds to: |
Ref document number: 14394 Country of ref document: AT Date of ref document: 19850815 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3264858 Country of ref document: DE Date of ref document: 19850829 |
|
| ET | Fr: translation filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19860310 Year of fee payment: 5 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19870430 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19890405 Ref country code: AT Effective date: 19890405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19890406 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19890430 Ref country code: CH Effective date: 19890430 Ref country code: BE Effective date: 19890430 |
|
| BERE | Be: lapsed |
Owner name: STEEL CASTINGS RESEARCH AND TRADE ASSOCIATION Effective date: 19890430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19891101 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19891228 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19900103 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| EUG | Se: european patent has lapsed |
Ref document number: 82301782.7 Effective date: 19900412 |