CN218361595U - Pressure flitch guide type structure of punching a hole - Google Patents
Pressure flitch guide type structure of punching a hole Download PDFInfo
- Publication number
- CN218361595U CN218361595U CN202223031676.6U CN202223031676U CN218361595U CN 218361595 U CN218361595 U CN 218361595U CN 202223031676 U CN202223031676 U CN 202223031676U CN 218361595 U CN218361595 U CN 218361595U
- Authority
- CN
- China
- Prior art keywords
- punch
- punching
- guide
- press
- base body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Landscapes
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
Abstract
本实用新型公开了一种压料板引导型冲孔结构,具有:下模座本体;凹模,安装在下模座本体上;压料板本体,安装上模上,压料板本体能够与下模座本体适配压紧冲裁零件;安装孔,设置在压料板本体内,安装孔倾斜设置;冲头,安装在安装孔内,冲头的第一端能够伸出压料板本体并与凹模适配;驱动块,滑动安装在安装孔内,驱动块能够驱动冲头运动;驱动块上端能够伸出压料板本体;上模座本体,能够上下运动;打杆,安装在上模座本体上,打杆能够驱动该驱动块滑动,结构紧凑,弥补大角度冲孔正向冲压集成开发空白,提高了产品冲裁精度。
The utility model discloses a punching structure guided by a binder plate, which comprises: a lower mold base body; a die installed on the lower mold base body; The mold base body is adapted to press the blanking parts; the installation hole is arranged in the holder body, and the installation hole is arranged obliquely; the punch is installed in the installation hole, and the first end of the punch can extend out of the holder body and Adapt to the die; the drive block is slidably installed in the mounting hole, and the drive block can drive the punch to move; the upper end of the drive block can extend out of the binder plate body; the upper die base body can move up and down; the punching rod is installed on the upper On the mold base body, the driving rod can drive the drive block to slide, with a compact structure, which makes up for the gap in the integrated development of large-angle punching and forward stamping, and improves the punching accuracy of the product.
Description
技术领域technical field
本实用新型属于汽车技术领域,尤其涉及一种压料板引导型冲孔结构。The utility model belongs to the technical field of automobiles, in particular to a pressing plate guiding type punching structure.
背景技术Background technique
目前,模具要求结构简单、工序少、维护便捷、成本最低,工艺精简是制造能力体现。而作为非标大角度冲孔行业一直是空白,因角度太大标准件厂家未开发此种标准斜锲,需要冲此种非标大角度冲孔则需要增加额外工序迎合冲孔特定冲压方向,或者将公差放大,牺牲精度满足生产。At present, the mold requires simple structure, few processes, convenient maintenance, and the lowest cost, and the simplification of the process is the embodiment of manufacturing capacity. As a non-standard large-angle punching industry has been blank, because the angle is too large, standard parts manufacturers have not developed such a standard oblique wedge. If this kind of non-standard large-angle punching is required, additional processes need to be added to cater for the specific punching direction of the punching. Or enlarge the tolerance and sacrifice precision to meet production.
在实现本实用新型的过程中,实用新型人发现现有技术至少存在以下问题:In the process of realizing the utility model, the inventor of the utility model has found that the prior art has at least the following problems:
目前大角度标准斜锲开发无论是长、宽、高都比较庞大,无法布置在一般模具内部使用,一般产品冲孔距离比较紧凑,工艺集中。导致标准斜锲在此种冲裁环境下无生存空间。如果要解决此冲孔问题就必须增加特定工序或者降低产品精度,忽略掉冲孔法向与当前工序冲压角度夹角。At present, the development of large-angle standard wedges is too large in terms of length, width, and height, and cannot be arranged inside general molds. The punching distance of general products is relatively compact and the process is concentrated. As a result, the standard wedge has no living space in this blanking environment. If you want to solve this punching problem, you must add a specific process or reduce the product accuracy, ignoring the angle between the normal direction of the punching hole and the punching angle of the current process.
1.无此标准斜锲开发,定制斜楔较大,无法满足紧凑型冲孔。1. Without the development of this standard wedge, the customized wedge is too large to satisfy compact punching.
2.增加特定工序迎合冲孔角度,工艺繁琐,成本较高。2. Add a specific process to cater to the punching angle, the process is cumbersome and the cost is high.
3.牺牲产品精度,迎合制造。3. Sacrifice product precision to cater to manufacturing.
实用新型内容Utility model content
本实用新型所要解决的技术问题是提供一种结构紧凑,弥补大角度冲孔正向冲压集成开发空白,提高了产品冲裁精度的压料板引导型冲孔结构The technical problem to be solved by the utility model is to provide a compact structure, which makes up for the gap in the integrated development of large-angle punching and forward punching, and improves the punching precision of the product.
为了解决上述技术问题,本实用新型所采用的技术方案是:一种压料板引导型冲孔结构,具有:In order to solve the above-mentioned technical problems, the technical solution adopted by the utility model is: a pressing plate-guided punching structure, which has:
下模座本体;Lower mold base body;
凹模,安装在所述下模座本体上;Die, installed on the body of the lower die holder;
压料板本体,安装上模上,所述压料板本体能够与所述下模座本体适配压紧冲裁零件;The binder plate body is installed on the upper die, and the binder plate body can be adapted to the lower die holder body to press the blanking parts;
安装孔,设置在所述压料板本体内,所述安装孔倾斜设置;The installation hole is arranged in the main body of the pressure plate, and the installation hole is arranged obliquely;
冲头,安装在所述安装孔内,所述冲头的第一端能够伸出所述压料板本体并与凹模适配;The punch is installed in the mounting hole, and the first end of the punch can protrude from the binder body and adapt to the die;
驱动块,滑动安装在所述安装孔内,所述驱动块能够驱动所述冲头运动;所述驱动块上端能够伸出压料板本体;The driving block is slidably installed in the installation hole, and the driving block can drive the punch to move; the upper end of the driving block can protrude from the binder plate body;
上模座本体,能够上下运动;The body of the upper die base can move up and down;
打杆,安装在所述上模座本体上,所述打杆能够驱动所述驱动块滑动。The punching rod is installed on the body of the upper die holder, and the punching rod can drive the sliding of the driving block.
所述压料板本体内还设有引导机构,所述引导机构包括引导轴,所述引导轴与安装孔适配并能在安装孔内滑动,所述冲头安装在引导轴上。A guide mechanism is also provided in the binder body, and the guide mechanism includes a guide shaft, which is adapted to the installation hole and can slide in the installation hole, and the punch is installed on the guide shaft.
所述压料板本体上还是设有限位所述驱动块行程的限位块。The clamping plate body is further provided with a limit block for limiting the stroke of the driving block.
所述压料板本体内还设有回位机构,所述回位机构为弹簧,所述弹簧套装在冲头上,所述弹簧的第一端与引导轴接触,第二端与压料板本体的内壁接触。The presser plate body is also provided with a return mechanism, the return mechanism is a spring, the spring is set on the punch, the first end of the spring is in contact with the guide shaft, and the second end is in contact with the presser plate contact with the inner wall of the body.
所述上模座本体安装压机滑块上。The upper die base body is installed on the press slide block.
所述下模座本体安装在压机工作台上。The lower mold base body is installed on the press table.
所述打杆通过螺栓可拆卸安装在所述上模座本体上。The punching rod is detachably mounted on the upper die base body through bolts.
一种上述的压料板引导型冲孔结构的使用方法,包括如下步骤:A method of using the above-mentioned binder plate-guided punching structure, comprising the following steps:
1)压机开始往下闭合,带动整个上模部分往下运动;1) The press starts to close downwards, driving the entire upper mold part to move downwards;
2)压料板首先接触放有材料零件的下模,当压料接触板料时上模弹簧开始压缩,压料板本体对冲裁零件施加压料力;2) The pressing plate first contacts the lower die with the material parts placed, and when the pressing material touches the sheet, the spring of the upper die starts to compress, and the pressing plate body exerts a pressing force on the punched parts;
3)当驱动块接触打杆时,驱动块将压机竖直方向力转化为冲裁方向力传递给冲头和引导轴;3) When the driving block contacts the punching rod, the driving block converts the vertical force of the press into the punching direction force and transmits it to the punch and the guide shaft;
4)引导轴与冲头固定,引导轴与压料板本体滑动配合,为冲头提供导向,同时引导轴压缩弹簧,压机持续往下运动;4) The guide shaft and the punch are fixed, and the guide shaft slides and cooperates with the binder body to provide guidance for the punch. At the same time, the guide shaft compresses the spring, and the press continues to move downward;
5)冲头挤出压料板本体开始对板料冲裁做工,并与凹模配合冲裁出形状;5) The punch extrudes the body of the pressing plate to start punching the sheet, and cooperates with the die to punch out the shape;
6)直到压机到达下死点,整个冲裁动作结束。6) Until the press reaches the bottom dead point, the whole punching action ends.
压机下行到达下死点后,压机工作台开始向上回程运动,上模弹簧为压料板本体提供卸料支撑,弹簧为冲头提供冲裁法向回程力,压料板本体压住冲裁板料,冲头开始往压料板本体内部回程,并退出冲入冲裁零件,引导轴为冲头提供回程导向,当回退后驱动块与限位块接触,限位块对其运动限位,防止驱动块、引导轴、冲头退出压料板本体;压机持续向上回程;受限位块限位停止向上运动,打杆与限位块脱离结束,然后上模弹簧压缩形成回程完毕,再上模运动完毕,直至压机到达上死点完成一次循环。After the press moves down to the bottom dead point, the press table starts to move upwards. The spring of the upper die provides support for the unloading of the press plate body, and the spring provides the normal return force for the punch. The press plate body presses the punch. When cutting the sheet, the punch starts to return to the inside of the pressing plate body, and exits to punch into the punched parts. The guide shaft provides the return guide for the punch. When the back is back, the driving block contacts the limit block, and the limit block moves against it. The limit prevents the drive block, guide shaft, and punch from exiting the clamping plate body; the press continues to return upward; the limit block stops the upward movement, the punching rod and the limit block are separated, and then the spring of the upper die is compressed to form a return stroke Finished, and then the movement of the upper mold is completed until the press reaches the upper dead center to complete a cycle.
上述技术方案中的一个技术方案具有如下优点或有益效果,One of the above technical solutions has the following advantages or beneficial effects,
1.工艺精简,结构简单紧凑,维护便捷,工序低,成本低廉,提高了整体工艺水平;1. The process is simplified, the structure is simple and compact, the maintenance is convenient, the process is low, the cost is low, and the overall process level is improved;
2.弥补大角度冲孔正向冲压集成开发空白;2. Make up for the gap in the integrated development of large-angle punching and forward stamping;
3.提高了产品冲裁精度。3. Improve the punching precision of the product.
附图说明Description of drawings
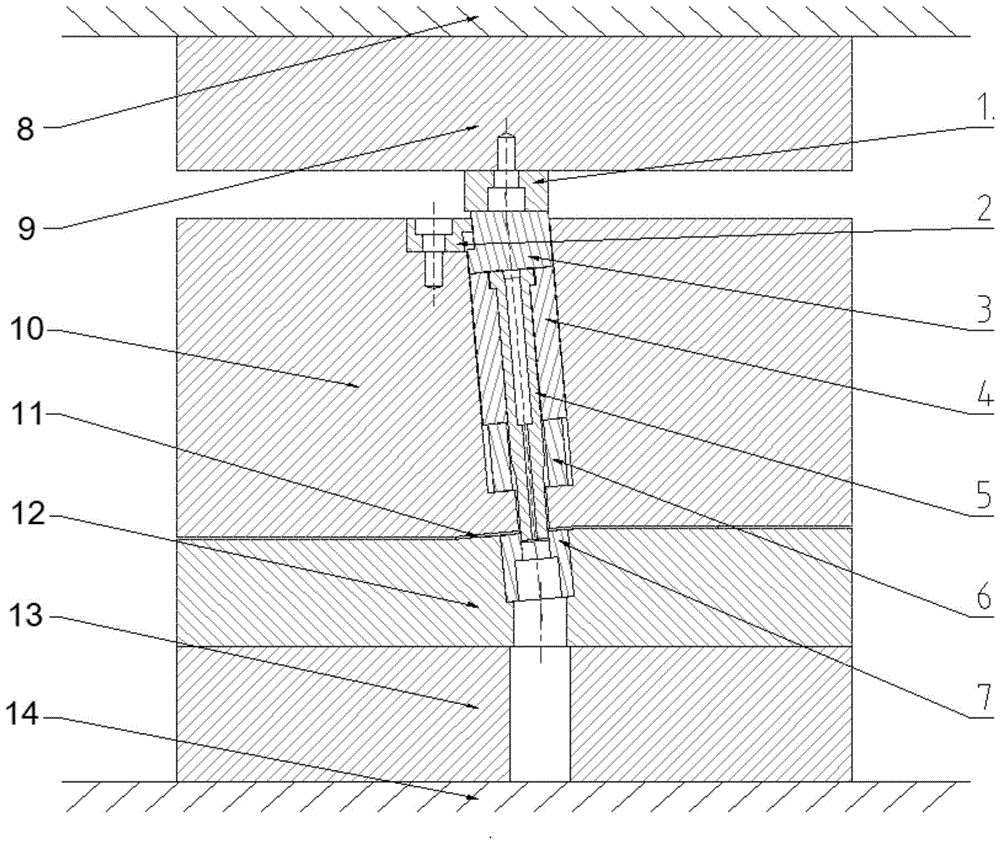
图1为本实用新型实施例中提供的压料板引导型冲孔结构的结构示意图;Fig. 1 is a structural schematic diagram of a binder plate-guided punching structure provided in an embodiment of the present invention;
上述图中的标记均为:1、打杆,2、限位块,3、驱动块,4、引导轴,5、冲头,6、弹簧,7、凹模,8、压机滑块,9、上模座本体,10、压料板本体,11、冲裁零件,12、下模板本体,13、下模座本体,14、压机工作台。The marks in the above figures are: 1. Punching rod, 2. Limiting block, 3. Driving block, 4. Guide shaft, 5. Punch, 6. Spring, 7. Die, 8. Press slider, 9. Upper die holder body, 10. Binder body, 11. Punched parts, 12. Lower die holder body, 13. Lower die holder body, 14. Press table.
具体实施方式Detailed ways
下面将结合本实用新型实施例中的附图,对本实用新型实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本实用新型一部分实施例,而不是全部的实施例。基于本实用新型中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本实用新型保护的范围。The technical solutions in the embodiments of the present invention will be clearly and completely described below in conjunction with the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only part of the embodiments of the present invention, not all of them. example. Based on the embodiments of the present utility model, all other embodiments obtained by persons of ordinary skill in the art without making creative efforts belong to the scope of protection of the present utility model.
参见图1,一种压料板引导型冲孔结构,具有:Referring to Figure 1, a binder-guided punching structure has:
下模座本体;凹模,安装在下模座本体上;“凹模”固定在下模本体中,作用是配合冲头冲出想要形状。The lower die holder body; the concave die is installed on the lower die holder body; the "die" is fixed in the lower die holder body, and its function is to cooperate with the punch to punch out the desired shape.
压料板本体,安装上模上,压料板本体能够与下模座本体适配压紧冲裁零件;安装孔,设置在压料板本体内,安装孔倾斜设置;倾斜设置形成冲头的倾斜运动,适应特殊大角度冲孔。The binder body is installed on the upper die, and the binder body can be adapted to the lower die base body to press the punched parts; the installation hole is arranged in the binder body, and the installation hole is set obliquely; the oblique setting forms the punch Tilt movement, suitable for special large-angle punching.
冲头,安装在安装孔内,冲头的第一端能够伸出压料板本体并与凹模适配;“标准冲头”作用是配合“凹模”冲出想要的形状。Punch, installed in the installation hole, the first end of the punch can extend out of the binder body and fit with the die; the function of the "standard punch" is to match the "die" to punch out the desired shape.
驱动块,滑动安装在安装孔内,驱动块能够驱动冲头运动;驱动块上端能够伸出压料板本体;“驱动块”作用是将“打杆”传递垂直方向力转化为想要的冲裁方向力。The driving block is slidably installed in the mounting hole. The driving block can drive the punch to move; the upper end of the driving block can protrude from the clamping plate body; the function of the "driving block" is to convert the vertical force transmitted by the "hitting rod" into the desired punch. Cut direction force.
上模座本体,能够上下运动;起到驱动作用。The body of the upper die base can move up and down; it plays a driving role.
打杆,安装在上模座本体上,打杆能够驱动该驱动块滑动,“打杆”通过螺栓反锁在上模座本体上,其作用是传递压机垂直方向力。The driving rod is installed on the body of the upper die base. The driving rod can drive the driving block to slide. The "driving rod" is locked on the upper die base body through bolts, and its function is to transmit the vertical force of the press.
主要原理:“打杆”传递压机竖直方向力给“驱动块”,由“驱动块”将竖直方向转化为产品垂直方向力并将力传递给“标准冲头”,然后由“标准冲头”配合“凹模”开展冲裁。The main principle: the "rod" transmits the vertical force of the press to the "drive block", and the "drive block" converts the vertical direction into the vertical force of the product and transmits the force to the "standard punch", and then the "standard punch" Punch" cooperates with "die" to carry out blanking.
压料板本体内还设有引导机构,引导机构包括引导轴,引导轴与安装孔适配并能在安装孔内滑动,冲头安装在引导轴上。“引导轴”作用是对“标准冲头”进行固定同时通过与压料板相对滑动为冲头提供运动导向作用,同时传递下方“标准弹簧”回程和预压力。A guide mechanism is also provided in the binder body, and the guide mechanism includes a guide shaft, which is adapted to the installation hole and can slide in the installation hole, and the punch is installed on the guide shaft. The role of the "guide shaft" is to fix the "standard punch" and provide movement guidance for the punch by sliding relative to the clamping plate, and at the same time transmit the return stroke and preload of the "standard spring" below.
压料板本体上还是设有限位驱动块行程的限位块。“限位块”主要起辅助作用,对“驱动快”、“引导轴”、“标准冲头”提供回程限位,并为该机构提供预压限位,防止晃动,该零件锁付在压料板本体中。The clamping plate body is still provided with a limiting block for limiting the stroke of the driving block. The "limit block" mainly plays an auxiliary role, providing return limit for "driver", "guide shaft" and "standard punch", and providing pre-compression limit for the mechanism to prevent shaking. in the sheet body.
压料板本体内还设有回位机构,回位机构为弹簧,弹簧套装在冲头上,弹簧的第一端与引导轴接触,第二端与压料板本体的内壁接触。“标准弹簧”通过“引导轴”与压料板本体相对挤压形成反向力,作用是为整个机构提供回程力。The binder body is also provided with a return mechanism, the return mechanism is a spring, the spring is sleeved on the punch, the first end of the spring is in contact with the guide shaft, and the second end is in contact with the inner wall of the binder body. The "standard spring" is pressed against the pressure plate body through the "guide shaft" to form a reverse force, and the function is to provide the return force for the whole mechanism.
上模座本体安装压机滑块上。下模座本体安装在压机工作台上。打杆通过螺栓可拆卸安装在上模座本体上。The upper die base body is installed on the slider of the press. The lower mold base body is installed on the press table. The punching rod is detachably mounted on the upper die base body through bolts.
弥补传统结构不能实现而设计的新型结构,从装配示意图可以看到非常紧凑,它能隐藏在压料板内安装并不会增加模具高度,其次占用面积就是引导轴大小,比标准冲头大一倍空间即可,根据安装孔加工角度不同,适应所有特殊大角度冲孔,无需增加工序或者降低产品精度来迎合冲裁。The new structure designed to make up for the failure of the traditional structure can be seen from the assembly schematic diagram, which is very compact. It can be hidden in the binder plate and installed without increasing the height of the mold. Secondly, the occupied area is the size of the guide shaft, which is one size larger than the standard punch. According to the different processing angles of the installation holes, it is suitable for all special large-angle punching holes, and there is no need to increase the process or reduce the product precision to meet the punching.
一种上述的压料板引导型冲孔结构的使用方法,包括如下步骤:A method of using the above-mentioned binder plate-guided punching structure, comprising the following steps:
1)压机开始往下闭合,带动整个上模部分往下运动;1) The press starts to close downwards, driving the entire upper mold part to move downwards;
2)压料板首先接触放有材料零件的下模,当压料接触板料时上模弹簧开始压缩,压料板本体对冲裁零件施加压料力;2) The pressing plate first contacts the lower die with the material parts placed, and when the pressing material touches the sheet, the spring of the upper die starts to compress, and the pressing plate body exerts a pressing force on the punched parts;
3)当驱动块接触打杆时,驱动块将压机竖直方向力转化为冲裁方向力传递给冲头和引导轴;3) When the driving block contacts the punching rod, the driving block converts the vertical force of the press into the punching direction force and transmits it to the punch and the guide shaft;
4)引导轴与冲头固定,引导轴与压料板本体滑动配合,为冲头提供导向,同时引导轴压缩弹簧,压机持续往下运动;4) The guide shaft and the punch are fixed, and the guide shaft slides and cooperates with the binder body to provide guidance for the punch. At the same time, the guide shaft compresses the spring, and the press continues to move downward;
5)冲头挤出压料板本体开始对板料冲裁做工,并与凹模配合冲裁出形状;5) The punch extrudes the body of the pressing plate to start punching the sheet, and cooperates with the die to punch out the shape;
6)直到压机到达下死点,整个冲裁动作结束。6) Until the press reaches the bottom dead point, the whole punching action ends.
压机下行到达下死点后,压机工作台开始向上回程运动,上模弹簧为压料板本体提供卸料支撑,弹簧为冲头提供冲裁法向回程力,压料板本体压住冲裁板料,冲头开始往压料板本体内部回程,并退出冲入冲裁零件,引导轴为冲头提供回程导向,当回退后驱动块与限位块接触,限位块对其运动限位,防止驱动块、引导轴、冲头退出压料板本体;压机持续向上回程;受限位块限位停止向上运动,打杆与限位块脱离结束,然后上模弹簧压缩形成回程完毕,再上模运动完毕,直至压机到达上死点完成一次循环。After the press moves down to the bottom dead point, the press table starts to move upwards. The spring of the upper die provides support for the unloading of the press plate body, and the spring provides the normal return force for the punch. The press plate body presses the punch. When cutting the sheet, the punch starts to return to the inside of the pressing plate body, and exits to punch into the punched parts. The guide shaft provides the return guide for the punch. When the back is back, the driving block contacts the limit block, and the limit block moves against it. The limit prevents the drive block, guide shaft, and punch from exiting the clamping plate body; the press continues to return upward; the limit block stops the upward movement, the punching rod and the limit block are separated, and then the spring of the upper die is compressed to form a return stroke Finished, and then the movement of the upper mold is completed until the press reaches the upper dead center to complete a cycle.
采用上述的结构后,此种冲裁方案和冲裁结构设计非常紧凑和科学弥补行业空白,适用不同角度冲压环境只需要调整相应安装孔角度即可。After adopting the above-mentioned structure, the punching scheme and punching structure design are very compact and scientifically make up for the gap in the industry. It is only necessary to adjust the angle of the corresponding installation hole to apply to the punching environment at different angles.
1.工艺精简,结构简单紧凑,维护便捷,工序低,成本低廉,提高了整体工艺水平;1. The process is simplified, the structure is simple and compact, the maintenance is convenient, the process is low, the cost is low, and the overall process level is improved;
2.弥补大角度冲孔正向冲压集成开发空白;2. Make up for the gap in the integrated development of large-angle punching and forward stamping;
3.提高了产品冲裁精度。3. Improve the punching precision of the product.
在本实用新型的描述中,需要理解的是,术语“同轴”、“底部”、“一端”、“顶部”、“中部”、“另一端”、“上”、“一侧”、“顶部”、“内”、“前部”、“中央”、“两端”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述本实用新型和简化描述,而不是指示或暗示所指的装置或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本实用新型的限制。In the description of the present utility model, it should be understood that the terms "coaxial", "bottom", "one end", "top", "middle", "other end", "upper", "one side", " The orientation or positional relationship indicated by "top", "inner", "front", "central", "both ends" etc. is based on the orientation or positional relationship shown in the drawings, and is only for the convenience of describing the utility model and simplifying the description , rather than indicating or implying that the device or element referred to must have a specific orientation, be constructed and operated in a specific orientation, and therefore should not be construed as limiting the utility model.
在本实用新型中,除非另有明确的规定和限定,术语“安装”、“设置”、“连接”、“固定”、“旋接”等术语应做广义理解,例如,可以是固定连接,也可以是可拆卸连接,或成一体;可以是机械连接,也可以是电连接;可以是直接相连,也可以通过中间媒介间接相连,可以是两个元件内部的连通或两个元件的相互作用关系,除非另有明确的限定,对于本领域的普通技术人员而言,可以根据具体情况理解上述术语在本实用新型中的具体含义。In this utility model, unless otherwise clearly specified and limited, terms such as "installation", "setting", "connection", "fixation" and "rotation" should be understood in a broad sense, for example, it may be a fixed connection, It can also be detachable connection, or integrated; it can be mechanical connection or electrical connection; it can be directly connected or indirectly connected through an intermediary, and it can be the internal communication of two components or the interaction of two components Unless otherwise clearly defined, those skilled in the art can understand the specific meanings of the above terms in the present utility model according to specific situations.
尽管已经示出和描述了本实用新型的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本实用新型的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本实用新型的范围由所附权利要求及其等同物限定。Although the embodiments of the present invention have been shown and described, those skilled in the art can understand that various changes and modifications can be made to these embodiments without departing from the principle and spirit of the present invention , replacements and modifications, the scope of the present utility model is defined by the appended claims and their equivalents.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223031676.6U CN218361595U (en) | 2022-11-15 | 2022-11-15 | Pressure flitch guide type structure of punching a hole |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223031676.6U CN218361595U (en) | 2022-11-15 | 2022-11-15 | Pressure flitch guide type structure of punching a hole |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218361595U true CN218361595U (en) | 2023-01-24 |
Family
ID=84938283
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202223031676.6U Active CN218361595U (en) | 2022-11-15 | 2022-11-15 | Pressure flitch guide type structure of punching a hole |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218361595U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115889572A (en) * | 2022-11-15 | 2023-04-04 | 宜宾凯翼汽车有限公司 | A binder-guided punching structure and method of use thereof |
-
2022
- 2022-11-15 CN CN202223031676.6U patent/CN218361595U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115889572A (en) * | 2022-11-15 | 2023-04-04 | 宜宾凯翼汽车有限公司 | A binder-guided punching structure and method of use thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204867060U (en) | Punch press with cutting device | |
| CN111842664A (en) | Lateral stamping unit for automotive parts | |
| CN201227671Y (en) | Automobile roof skylight punched hole switch-over mechanism in perforating die | |
| CN212285529U (en) | Workpiece shearing, punching and bending compound die | |
| CN206105999U (en) | Die -cut first adjustable die cutting machine | |
| CN107052137A (en) | A kind of brake dust side-cutting die | |
| CN110064702A (en) | One kind being used for the stamping forming composable mold of outer covering piece and its moulding process | |
| CN205833930U (en) | A kind of hand pressure blanking units | |
| CN115889572A (en) | A binder-guided punching structure and method of use thereof | |
| CN120133379A (en) | Fine stamping die for step parts forming | |
| CN216801367U (en) | Anti-deviation hardware stamping die | |
| CN220387582U (en) | Hinge punching press crimping device | |
| CN102974733B (en) | A kind of vehicle oil filler small door hinge axle cold upsetting die of car | |
| CN217748961U (en) | Thinning mechanism | |
| CN207103557U (en) | Small bellows punch mechanism | |
| CN211888634U (en) | Movable punching mechanism of stamping die | |
| CN113751579B (en) | Micropore blanking die | |
| CN221848368U (en) | High-speed punching die structure that can extend service life | |
| CN221952179U (en) | Material structure is taken off to mould | |
| CN209223065U (en) | Automobile engine adjusting pad piece progressive die blanking apparatus | |
| CN220216459U (en) | Stamping die compound die detection mechanism | |
| CN223997161U (en) | A stamping stripping device | |
| CN216095857U (en) | Metal mold tool | |
| CN217964423U (en) | Quick riveting shell mechanism | |
| CN218255609U (en) | A silicone pad blanking jig |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| PE01 | Entry into force of the registration of the contract for pledge of patent right |
Denomination of utility model: A guiding punching structure for pressure plate Granted publication date: 20230124 Pledgee: Yibin Development Holding Group Co.,Ltd. Pledgor: YIBIN COWIN AUTO Co.,Ltd. Registration number: Y2025510000054 |
|
| PE01 | Entry into force of the registration of the contract for pledge of patent right |