CN218015100U - Rib pressing device for metal cylinder body - Google Patents
Rib pressing device for metal cylinder body Download PDFInfo
- Publication number
- CN218015100U CN218015100U CN202222646272.1U CN202222646272U CN218015100U CN 218015100 U CN218015100 U CN 218015100U CN 202222646272 U CN202222646272 U CN 202222646272U CN 218015100 U CN218015100 U CN 218015100U
- Authority
- CN
- China
- Prior art keywords
- support
- driven voller
- ring
- mounting box
- metal cylinder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 239000002184 metal Substances 0.000 title claims abstract description 18
- 238000003825 pressing Methods 0.000 title abstract description 8
- 230000005540 biological transmission Effects 0.000 claims abstract description 5
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 abstract description 25
- 238000000034 method Methods 0.000 abstract description 5
- 230000001105 regulatory effect Effects 0.000 abstract 1
- 230000006835 compression Effects 0.000 description 5
- 238000007906 compression Methods 0.000 description 5
- 230000003014 reinforcing effect Effects 0.000 description 3
- 230000004323 axial length Effects 0.000 description 2
- 210000003205 muscle Anatomy 0.000 description 2
- 230000007306 turnover Effects 0.000 description 2
- 238000010586 diagram Methods 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000010030 laminating Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 230000002265 prevention Effects 0.000 description 1
- 238000005096 rolling process Methods 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 230000001360 synchronised effect Effects 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images
Landscapes
- Press Drives And Press Lines (AREA)
Abstract
The utility model relates to a vertical metal water tank processing technology field, very much relate to a metal drum barrel beading device, include by setting up the support on the quick-witted case and with drive roll and the driven voller that the roll body of support upper roll seat assembly constitutes, drive roll and driven voller are upper and lower and the roll body sets up relatively, still be equipped with on the support of driven voller and prevent inclined to one side mechanism, prevent inclined to one side mechanism difference fixed connection driven voller's support and the mounting box of quick-witted case, set firmly the guiding tube that is located support both sides and parallel support on the mounting box, the one end that slides on the guiding tube body of rod and is equipped with the spacing ring and keeps away from the mounting box rotates and is equipped with the holding ring, be equipped with the regulating assembly to spacing ring transmission in the mounting box. The utility model discloses simple structure can carry out spacing regulation to not unidimensional barrel, ensures that the barrel is rotating the no off tracking phenomenon of bar pressing in-process, ensures high efficiency, the accurate nature of bar pressing operation.
Description
Technical Field
The utility model relates to a vertical metal water tank processing technology field, very much relate to a metal drum barrel ribbing device.
Background
The vertical metal water tank is mainly used for water storage of a top layer of a building, the volume of the vertical metal water tank is large, but the wall thickness of a used plate is thin, and a plurality of cylinders are basically formed by butt welding, so that in order to improve the structural strength of the vertical metal water tank, rib pressing operation needs to be carried out on a formed cylinder body, namely a plurality of reinforcing rib structures are formed by annularly rolling the cylinder wall of the cylinder body. The existing ribbing technology is mature, but when the ribbing technology is applied to a water tank, the following problems exist: the purpose of labor and time saving is achieved, the length of the compression roller is designed to be large, multiple reinforcing ribs can be extruded at one time, but the axial lengths of the water tank cylinders with different sizes are different, so that the length of the compression roller cannot be completely matched with the length of all the cylinders, if the length of the cylinder is smaller than the length of the compression roller, the initial installation position of the cylinder box compression roller is inclined, the reinforcing ribs formed after the compression roller is operated are not in a perfect circle but in a spiral line, materials are scrapped, and high requirements are provided for the skill and proficiency of operators.
SUMMERY OF THE UTILITY MODEL
The utility model discloses a metal drum barrel beading device that just lies in solving above-mentioned problem and propose, the utility model discloses simple structure can carry out spacing regulation to unidimensional barrel, ensures that the barrel does not have the off tracking phenomenon rotating beading in-process, ensures high-efficient, the accurate nature of beading operation.
The utility model provides a metal drum barrel beading device, includes by setting up the support on the quick-witted case and with the drive roll and the driven voller that the roll body of support upper roll seat assembly is constituteed, drive roll and driven voller be upper and lower and the roll body sets up relatively, still be equipped with on the support of driven voller and prevent inclined to one side mechanism, prevent inclined to one side mechanism support and the mounting box of quick-witted case of fixed connection driven voller respectively, set firmly the guiding tube that is located support both sides and parallel support on the mounting box, the one end that slides on the guiding tube body of rod and be equipped with the spacing ring and keep away from the mounting box rotates and is equipped with the holding ring, be equipped with the driven adjusting part to the spacing ring in the mounting box. Through setting up the deviation prevention mechanism, staff's accessible adjusting part removes the spacing ring, makes holding ring and spacing ring inject the orbit of water tank barrel in following the rotation of initiative, driven voller circumference pressure muscle jointly, prevents the emergence of water tank barrel skew phenomenon effectively to improve the pressure muscle precision to the water tank barrel.
Preferably, a motor for driving the roller body of the driving roller is arranged in the case, and a hydraulic cylinder for vertically driving the upper roller seat is arranged on the support of the driving roller. The pneumatic cylinder can carry out vertical position control to the roller seat and the roll body of drive roll for the water tank barrel can be placed fast on the roll body of driven voller and afterwards by drive roll and driven voller cooperation centre gripping.
Preferably, the guide tube is provided with an indication groove, and the bottom wall of the indication groove is provided with length scale marks. The setting of length scale mark on the instruction groove can conveniently adjust the position of spacing ring and stand pipe, and then realizes coming the working distance of quick adjustment spacing ring and holding ring according to the water tank barrel size of treating processing.
Preferably, the adjusting assembly comprises a servo motor arranged in the mounting box, an output shaft of the servo motor is fixedly connected with a worm, a threaded rod is rotationally arranged in the guide tube, and one end of the threaded rod penetrates into the mounting box and is provided with a worm wheel in meshing transmission with the worm;
the guiding tube body is axially provided with a notch, and a sliding block in sliding fit with the notch is in threaded fit with the threaded rod.
Preferably, the inner ring surface of the limit ring is assembled with the outer ring body of the bearing, and the inner ring body of the bearing is connected with the sliding block. The servo motor realizes the rotation of the threaded rod through the transmission of the worm and gear, the sliding block is limited by the notch and cannot rotate along with the threaded rod, and only can axially move relative to the threaded rod, so that the limiting ring is driven to move through the bearing. The setting up of bearing makes the spacing ring take place to have enough to meet the need relatively the stand pipe, therefore spacing ring and holding ring are providing the spacing basis of axial to water tank barrel axial both ends for spacing ring and holding ring can be along with the turnover of water tank barrel and the synchronous turnover, thereby realize providing spacingly to the beading operation process of water tank barrel.
Preferably, the corners of the positioning ring and the limiting ring are both rounded. The setting of chamfer can be so that holding ring and spacing ring can have effectively laminating water tank barrel terminal surface.
The utility model has the advantages that: the utility model discloses simple structure can carry out spacing regulation to unidimensional barrel, ensures that the barrel is rotating the no off tracking phenomenon of rib pressing in-process, ensures high efficiency, the accurate nature of rib pressing operation.
Drawings
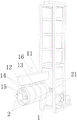
Fig. 1 is a schematic structural view of the beading device of the present invention;
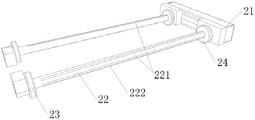
fig. 2 is a schematic structural view of the deviation preventing mechanism of the present invention;
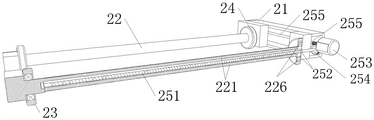
fig. 3 is the schematic diagram of the internal structure of the deviation preventing mechanism of the present invention.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
In the specific implementation: as shown in fig. 1-3, a metal cylinder ribbing device includes a driving roller 14 and a driven roller 15, which are composed of a support 11 disposed on a chassis 1 and a roller body 13 assembled with a roller seat 12 on the support 11, the driving roller 14 and the driven roller 15 are disposed up and down with the roller bodies opposite to each other, a motor for driving the roller body 13 of the driving roller 14 is disposed in the chassis 1, and a hydraulic cylinder 16 for vertically driving the roller seat 12 is disposed on the support 11 of the driving roller 14.
Still be equipped with on the support 11 of driven voller 15 and prevent inclined to one side mechanism 2, prevent inclined to one side mechanism 2 and be fixed connection driven voller 15's support 11 and quick-witted case 1's mounting box 21 respectively, set firmly the guiding tube 22 that is located 11 both sides of support and parallel support 11 on the mounting box 21, the one end rotation that the guiding tube 22 body of rod was gone up to slide and is equipped with spacing ring 24 and keeps away from mounting box 21 is equipped with holding ring 23, the corner of holding ring 23 and spacing ring 24 all has the fillet.
An adjusting component for transmitting the limiting ring 24 is arranged in the mounting box 21 and comprises a servo motor 253 arranged in the mounting box 21, an output shaft of the servo motor 253 is fixedly connected with a worm 255, a threaded rod 251 is rotationally arranged in the guide tube 22, and one end of the threaded rod 251 penetrates into the mounting box 21 and is provided with a worm wheel 254 in meshing transmission with the worm 255; a notch 221 is axially formed in the tube body of the guide tube 22, and a sliding block 252 in sliding fit with the notch 221 is in threaded fit with the threaded rod 251. The inner ring surface of the limit ring 24 is assembled with the outer ring body of the bearing 226, and the inner ring body of the bearing 226 is connected with the sliding block 252.
The guide tube 22 is provided with an indication groove 222, and the bottom wall of the indication groove 222 is provided with length scale marks.
The utility model discloses when using, the staff carries out spacing ring 24's position adjustment according to the axial length of waiting to process the water tank barrel, open servo motor 253, servo motor 253 drives worm 255 rotatory, worm 255 drives two worm wheel 254 simultaneously rotatory, worm wheel 254 drives threaded rod 251 rotatory, threaded rod 251 drives slider 252 rotatory, because slider 252 and breach 221 cooperation, so breach 221 prevents that slider 252 from following threaded rod 251 and rotating together, make slider 252 can only drive to drive spacing ring 24 through bearing 226 and follow threaded rod 251 axial displacement and be close to holding ring 23, and judge the interval of holding ring 23 and spacing ring through the length scale mark in the instruction groove 222. Then the water tank barrel is sleeved on the support 11 of the driven roller 15 in a penetrating manner, the inner wall of the water tank barrel is supported by the roller body 13 of the driven roller 15, and the positioning ring 23 and the limiting ring 24 are attached to the two axial ends of the water tank barrel.
Then the hydraulic cylinder 16 drives the roller seat 12 and the roller body 13 of the driving roller 14 to move downwards and cooperate with the driven roller 15 to press and hold the water tank cylinder body. And starting a motor of the driving roller 14, enabling the driving roller 14 to be matched with the driven roller 15 to drive the water tank barrel to rotate, and simultaneously enabling the limiting ring 24 and the positioning ring 23 to synchronously rotate to prevent the water tank barrel from deviating, so that the driving roller 14 and the driven roller 15 press the water tank barrel into a plurality of annular pressing ribs.
Claims (6)
1. The utility model provides a metal drum barrel beading device, includes by setting up support (11) on quick-witted case (1) and with support (11) go up drive roll (14) and driven voller (15) that roll body (13) of roller seat (12) assembly constitute, drive roll (14) and driven voller (15) are upper and lower and the roll body sets up relatively, its characterized in that, still be equipped with on support (11) of driven voller (15) and prevent inclined to one side mechanism (2), prevent inclined to one side mechanism (2) respectively fixed connection driven voller (15) support (11) and quick-witted case (1) install box (21), install box (21) are last to set firmly guide tube (22) that are located support (11) both sides and parallel support (11), the one end that slides on the guide tube (22) body of rod is equipped with spacing ring (24) and keeps away from install box (21) rotates and is equipped with holding ring (23), be equipped with the driven adjusting part to spacing ring (24) in the install box (21).
2. The metal cylinder beading apparatus according to claim 1, wherein: a motor for driving a roller body (13) of a driving roller (14) is arranged in the case (1), and a hydraulic cylinder (16) for driving an upper roller seat (12) vertically is arranged on a support (11) of the driving roller (14).
3. The metal cylinder beading apparatus according to claim 1, wherein: the guide tube (22) is provided with an indicating groove (222), and the bottom wall of the indicating groove (222) is provided with length scale marks.
4. The metal cylinder beading apparatus according to claim 1, wherein: the adjusting assembly comprises a servo motor (253) arranged in the mounting box (21), an output shaft of the servo motor (253) is fixedly connected with a worm (255), a threaded rod (251) is rotatably arranged in the guide pipe (22), one end of the threaded rod (251) penetrates through the mounting box (21) and is provided with a worm wheel (254) in meshing transmission with the worm (255);
a notch (221) is axially formed in the tube body of the guide tube (22), and a sliding block (252) in sliding fit with the notch (221) is in threaded fit with the threaded rod (251).
5. The metal cylinder beading apparatus according to claim 4, wherein: the inner ring surface of the limiting ring (24) is assembled with the outer ring body of the bearing (226), and the inner ring body of the bearing (226) is connected with the sliding block (252).
6. The metal cylinder beading apparatus according to claim 1, wherein: the corners of the positioning ring (23) and the limiting ring (24) are rounded.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222646272.1U CN218015100U (en) | 2022-10-09 | 2022-10-09 | Rib pressing device for metal cylinder body |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222646272.1U CN218015100U (en) | 2022-10-09 | 2022-10-09 | Rib pressing device for metal cylinder body |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218015100U true CN218015100U (en) | 2022-12-13 |
Family
ID=84357578
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202222646272.1U Active CN218015100U (en) | 2022-10-09 | 2022-10-09 | Rib pressing device for metal cylinder body |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218015100U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117884500A (en) * | 2024-02-02 | 2024-04-16 | 广东元晟智能装备制造有限公司 | A vertical cylinder rib pressing machine |
-
2022
- 2022-10-09 CN CN202222646272.1U patent/CN218015100U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117884500A (en) * | 2024-02-02 | 2024-04-16 | 广东元晟智能装备制造有限公司 | A vertical cylinder rib pressing machine |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101786130B (en) | Internal stiffening loop thrust unit for CNC steel reinforcement cage molding machine | |
| CN210647896U (en) | Hydraulic automatic edge rolling machine convenient for loading and unloading | |
| CN212761842U (en) | Welding device for machining circular tube materials | |
| CN111389976A (en) | Universal seamless steel pipe bending machine | |
| CN222790262U (en) | Four-roller plate bending machine with symmetrical linkage | |
| CN219520076U (en) | Precise leveling machine | |
| CN219648459U (en) | Rolling device for processing polymer composite bearing | |
| CN220161208U (en) | Diagonal rolling device of steel bar sleeve thread rolling machine | |
| CN217191758U (en) | Tension leveler with adjustable compression roller height | |
| CN212292149U (en) | Coiling mechanism is used in sticky tape production | |
| CN201978978U (en) | Opening type automatic elevating four-roller rolling machine | |
| CN212019027U (en) | Seamless steel pipe bending machine | |
| CN211990377U (en) | Small-size portable forming mill | |
| CN212168706U (en) | Edge hole punching device for corrugated steel plate | |
| CN222428956U (en) | Plate bending machine convenient for feeding and adjusting and used for asphalt tank steel plate | |
| CN222519614U (en) | Double-station cold bending machine equipment | |
| CN210098590U (en) | Multi-diameter multi-layer thin-wall corrugated pipe circle calibration device | |
| CN221269286U (en) | Aluminum plate composite calendaring device | |
| CN219616425U (en) | A rolling machine for bearing processing | |
| CN221455796U (en) | Pipeline connecting device for hydraulic engineering | |
| CN217858907U (en) | Nonrust steel pipe location perforating device | |
| CN206445045U (en) | Steel plate edge rolling device | |
| CN222042090U (en) | A servo feeder | |
| CN215614196U (en) | High-efficient straightener of cold drawn pipe production | |
| CN219541364U (en) | Uncoiler with lifting mechanism for producing steel sheet pile |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |