CN216329906U - A kind of insert injection molding device of automobile tail lamp mask - Google Patents
A kind of insert injection molding device of automobile tail lamp mask Download PDFInfo
- Publication number
- CN216329906U CN216329906U CN202122741165.2U CN202122741165U CN216329906U CN 216329906 U CN216329906 U CN 216329906U CN 202122741165 U CN202122741165 U CN 202122741165U CN 216329906 U CN216329906 U CN 216329906U
- Authority
- CN
- China
- Prior art keywords
- cover half
- fixed die
- injection molding
- fixed
- die
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000001746 injection moulding Methods 0.000 title claims abstract description 36
- 230000007246 mechanism Effects 0.000 claims abstract description 29
- 238000002347 injection Methods 0.000 claims abstract description 27
- 239000007924 injection Substances 0.000 claims abstract description 27
- 238000001816 cooling Methods 0.000 claims abstract description 26
- 238000005485 electric heating Methods 0.000 claims abstract description 9
- 239000007788 liquid Substances 0.000 claims description 29
- 238000003860 storage Methods 0.000 claims description 14
- WYTGDNHDOZPMIW-RCBQFDQVSA-N alstonine Natural products C1=CC2=C3C=CC=CC3=NC2=C2N1C[C@H]1[C@H](C)OC=C(C(=O)OC)[C@H]1C2 WYTGDNHDOZPMIW-RCBQFDQVSA-N 0.000 claims description 3
- 238000000465 moulding Methods 0.000 claims description 3
- 239000002826 coolant Substances 0.000 claims description 2
- 239000004033 plastic Substances 0.000 claims description 2
- 229920003023 plastic Polymers 0.000 claims description 2
- 239000000463 material Substances 0.000 abstract description 13
- 238000002844 melting Methods 0.000 abstract description 4
- 230000008018 melting Effects 0.000 abstract description 4
- 239000000110 cooling liquid Substances 0.000 description 6
- 238000000034 method Methods 0.000 description 4
- 238000010438 heat treatment Methods 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000002994 raw material Substances 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000004512 die casting Methods 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
Images



Landscapes
- Moulds For Moulding Plastics Or The Like (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
Abstract
Description
技术领域technical field
本实用新型涉及注塑装置技术领域,尤其涉及一种汽车尾灯面罩的镶嵌注塑装置。The utility model relates to the technical field of injection molding devices, in particular to an inlaid injection molding device for automobile taillight masks.
背景技术Background technique
注塑是一种工业产品生产造型的方法,产品通常使用橡胶注塑和塑料注塑,注塑还可分注塑成型模压法和压铸法,而汽车尾灯的面罩在生产时就是采用镶嵌注塑的方法,在注塑时,先将原来的尾灯面罩放入模具的型腔中,然后使得动模与定模进行合模,再通过注射机构向型腔内注射镶嵌的物料。Injection molding is a method for the production and modeling of industrial products. Products usually use rubber injection molding and plastic injection molding. Injection molding can also be divided into injection molding molding method and die-casting method. The mask of automobile taillights is produced by insert injection molding method. When injection molding , first put the original taillight mask into the cavity of the mold, then make the movable mold and the fixed mold to close the mold, and then inject the inlaid material into the cavity through the injection mechanism.
但是现有的镶嵌注塑装置在使用过程中,物料进入定模的注塑通道或型腔内后温度就会下降,从而不能与原来的尾灯面罩进行完好的融合,最后成型时容易出现线缝。而如果让物料在定模内保持高温融化状态的话,则在注塑完成后需要更长的时间等待物料和原尾灯面罩冷却,从而减低了生产效率,因此本实用新型提出了一种汽车尾灯面罩的镶嵌注塑装置。However, during the use of the existing insert injection molding device, the temperature of the material will drop after entering the injection channel or cavity of the fixed mold, so that it cannot be completely integrated with the original taillight mask, and seams are prone to appear during the final molding. However, if the material is kept in a high temperature melting state in the fixed mold, it will take a longer time to wait for the material and the original taillight mask to cool after the injection molding is completed, thereby reducing the production efficiency. Therefore, the utility model proposes an automobile taillight mask. Insert injection molding device.
实用新型内容Utility model content
本实用新型的目的是为了解决现有技术中存在的缺点,而提出的一种汽车尾灯面罩的镶嵌注塑装置。The purpose of the utility model is to solve the shortcomings in the prior art, and proposes an inlay injection molding device for a car taillight mask.
为了实现上述目的,本实用新型采用了如下技术方案:一种汽车尾灯面罩的镶嵌注塑装置,包括滑轨结构,所述滑轨结构顶端设有第一定模和第二定模,且第一定模和第二定模内部结构完全相同,所述第一定模和第二定模的同侧设有动模,且动模远离第一定模和第二定模一侧连接有液压机,所述第一定模和第二定模远离动模一侧均单独连接有注射机构,所述第一定模和第二定模顶端均设有冷却机构,所述滑轨结构外侧壁固定有伺服电机,所述第一定模和第二定模靠近动模一侧均开设有型腔,且第一定模和第二定模内部靠近型腔处设有电加热板,所述第一定模和第二定模内部开设有注塑通道和冷却通道。In order to achieve the above purpose, the utility model adopts the following technical solutions: an inlay injection molding device for an automobile taillight mask, including a slide rail structure, the top of the slide rail structure is provided with a first fixed mold and a second fixed mold, and the first fixed mold The internal structures of the fixed die and the second fixed die are exactly the same, a movable die is arranged on the same side of the first fixed die and the second fixed die, and a hydraulic press is connected to the side of the movable die away from the first fixed die and the second fixed die, The first fixed mold and the second fixed mold are separately connected with the injection mechanism on the side away from the movable mold, the top of the first fixed mold and the second fixed mold are provided with a cooling mechanism, and the outer side wall of the slide rail structure is fixed with a cooling mechanism. Servo motor, the first fixed mold and the second fixed mold are provided with a cavity on the side close to the movable mold, and an electric heating plate is provided inside the first fixed mold and the second fixed mold near the cavity, and the first fixed mold and the second fixed mold are provided with an electric heating plate. An injection channel and a cooling channel are opened inside the fixed mold and the second fixed mold.
进一步的,所述滑轨结构包括U型底板,所述U型底板上表面靠近第一定模和第二定模一侧固定有第一轨道,所述第一轨道内部滑动连接有两个滑块,且两个滑块顶端分别与第一定模和第二定模底端固定连接,所述第一轨道内部转动连接有丝杆,且丝杆穿过两个滑块并与两个滑块螺纹转动连接,所述丝杆一端穿过U型底板侧壁与伺服电机驱动端固定连接,便于通过伺服电机的正反转动来带动第一定模和第二定模在滑轨结构顶端左右来回移动,便于动模轮流与第一定模和第二定模进行合模。Further, the sliding rail structure includes a U-shaped bottom plate, a first rail is fixed on the upper surface of the U-shaped bottom plate close to the first fixed die and the second fixed die, and two slides are slidably connected inside the first rail. and the top ends of the two sliders are respectively fixedly connected with the bottom ends of the first fixed die and the second fixed die, the first track is rotatably connected with a screw rod, and the screw rod passes through the two sliders and is connected with the two sliders. The block is screwed and connected, and one end of the screw rod is fixedly connected to the drive end of the servo motor through the side wall of the U-shaped bottom plate, which is convenient to drive the first fixed die and the second fixed die to the left and right at the top of the slide rail structure through the positive and negative rotation of the servo motor. Moving back and forth, it is convenient for the movable mold to take turns to close the mold with the first fixed mold and the second fixed mold.
进一步的,所述U型底板上表面靠近注射机构的一侧固定有第二轨道,所述注射机构底端固定有支撑杆,且支撑杆底端与第二轨道滑动连接,便于注射机构能与第一定模和第二定模共同移动。Further, a second rail is fixed on the side of the upper surface of the U-shaped base plate close to the injection mechanism, a support rod is fixed at the bottom end of the injection mechanism, and the bottom end of the support rod is slidably connected with the second rail, so that the injection mechanism can be connected with the injection mechanism. The first stationary mold and the second stationary mold move together.
进一步的,所述注塑通道两端分别与型腔和注射机构连通,使得注射机构内的物料可以通过注塑通道进入型腔内。Further, both ends of the injection molding channel are respectively communicated with the mold cavity and the injection mechanism, so that the material in the injection mechanism can enter the mold cavity through the injection molding channel.
进一步的,所述冷却机构包括储液箱和循环泵,且储液箱内部设有冷却液,所述储液箱的进液口与循环泵出液口分别连接有第一连接管和第二连接管,所述第一连接管和第二连接管另一端分别与冷却通道两端连通,所述储液箱出液口与循环泵进液口连通,便于通过循环泵将储液箱内的冷却液泵入冷却通道内,从而对第一定模或第二定模进行冷却,使得成型的物料能更快脱模。Further, the cooling mechanism includes a liquid storage tank and a circulating pump, and the liquid storage tank is provided with cooling liquid, and the liquid inlet of the liquid storage tank and the liquid outlet of the circulating pump are respectively connected with a first connecting pipe and a second connecting pipe. Connecting pipe, the other ends of the first connecting pipe and the second connecting pipe are respectively connected with both ends of the cooling channel, and the liquid outlet of the liquid storage tank is connected with the liquid inlet of the circulating pump, so that it is convenient to pass the circulating pump to the liquid storage tank. The cooling liquid is pumped into the cooling channel, so as to cool the first fixed mold or the second fixed mold, so that the molded material can be released from the mold faster.
进一步的,所述储液箱内部设有制冷器,可以对冷却液进行制冷,从而保证冷却液始终处于低温状态,可以更好的冷却第一定模和第二定模。Further, a refrigerator is provided inside the liquid storage tank, which can refrigerate the cooling liquid, so as to ensure that the cooling liquid is always in a low temperature state, and can better cool the first fixed mold and the second fixed mold.
进一步的,所述冷却通道为蛇形的弯曲通道,使得冷却通道内的冷却液可以与第一定模和第二定模内部接触面积更大,进而能更快的冷却第一定模和第二定模。Further, the cooling channel is a serpentine curved channel, so that the cooling liquid in the cooling channel can have a larger contact area with the inside of the first stationary mold and the second stationary mold, thereby cooling the first stationary mold and the second stationary mold faster. Two fixed molds.
本实用新型的有益效果:The beneficial effects of the present utility model:
本实用新型在使用时,通过设置滑轨结构、第一定模、第二定模、动模、液压机、冷却机构和伺服电机,第一定模和第二定模内部靠近型腔处均设有电加热板,因此在进行镶嵌注塑时,可以使得物料进入注塑通道和型腔内后仍能保持高温熔化状态,从而保证物料与原面罩之间融合的更好,不会出现线缝。另外,第一定模和第二定模上单独连接有注射机构,因此可以通过伺服电机带动第一定模和第二定模在滑轨结构上左右来回移动,使得动模可以轮流与第一定模和第二定模进行合模,从而增加第一定模或第二定模的冷却时间,提高注塑的效率同时,使得注塑产品可以冷却的更彻底,更有利于脱模。When the utility model is in use, by setting the slide rail structure, the first fixed mold, the second fixed mold, the movable mold, the hydraulic press, the cooling mechanism and the servo motor, the inside of the first fixed mold and the second fixed mold near the cavity are provided with There is an electric heating plate, so during insert injection molding, the material can still maintain a high temperature melting state after entering the injection channel and cavity, so as to ensure better fusion between the material and the original mask, and there will be no seams. In addition, the first fixed mold and the second fixed mold are independently connected with an injection mechanism, so the first fixed mold and the second fixed mold can be driven by the servo motor to move back and forth on the slide rail structure, so that the moving mold can take turns with the first fixed mold and the second fixed mold. The fixed mold and the second fixed mold are closed, thereby increasing the cooling time of the first fixed mold or the second fixed mold, improving the efficiency of injection molding, and at the same time, the injection molding product can be cooled more thoroughly, which is more conducive to demoulding.
附图说明Description of drawings
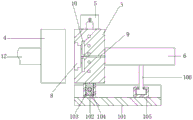
图1为本实用新型的俯视图;Fig. 1 is the top view of the utility model;
图2为本实用新型的侧剖图;Fig. 2 is the side sectional view of the utility model;
图3为本实用新型的第二定模剖视图;3 is a cross-sectional view of the second fixed die of the present utility model;
图4为本实用新型的第一定模剖视图。4 is a cross-sectional view of the first stationary die of the present invention.
图例说明:illustration:
1、滑轨结构;101、U型底板;102、第一轨道;103、滑块;104、丝杆;105、第二轨道;106、支撑杆;2、第一定模;3、第二定模;4、动模;5、冷却机构;51、储液箱; 52、循环泵;53、第一连接管;54、第二连接管;6、注射机构;7、伺服电机;8、型腔; 9、注塑通道;10、电加热板;11、冷却通道;12、液压机。1. Slide rail structure; 101, U-shaped bottom plate; 102, first track; 103, slider; 104, lead screw; 105, second track; 106, support rod; 2, first fixed mold; 3, second Fixed mold; 4. Moving mold; 5. Cooling mechanism; 51. Liquid storage tank; 52. Circulating pump; 53. First connecting pipe; 54. Second connecting pipe; 6. Injection mechanism; 7. Servo motor; 8. Cavity; 9. Injection channel; 10. Electric heating plate; 11. Cooling channel; 12. Hydraulic press.
具体实施方式Detailed ways
如图1-4所示,涉及一种汽车尾灯面罩的镶嵌注塑装置,包括滑轨结构1,滑轨结构1顶端设有第一定模2和第二定模3,且第一定模2和第二定模3内部结构完全相同,第一定模2和第二定模3的同侧设有动模4,且动模4远离第一定模2和第二定模3一侧连接有液压机12,第一定模2和第二定模3远离动模4一侧均单独连接有注射机构6,第一定模2和第二定模3顶端均设有冷却机构5,滑轨结构1外侧壁固定有伺服电机7,第一定模2和第二定模3靠近动模4一侧均开设有型腔8,且第一定模2和第二定模3内部靠近型腔8处设有电加热板10,第一定模2和第二定模3内部开设有注塑通道9和冷却通道11。As shown in Figures 1-4, it relates to an inlay injection molding device for an automobile taillight mask, comprising a
如图2和图3所示,滑轨结构1包括U型底板101,U型底板101上表面靠近第一定模2和第二定模3一侧固定有第一轨道102,第一轨道102内部滑动连接有两个滑块103,且两个滑块103顶端分别与第一定模2和第二定模3底端固定连接,第一轨道102内部转动连接有丝杆104,且丝杆104穿过两个滑块103并与两个滑块103螺纹转动连接,丝杆104一端穿过U型底板101侧壁与伺服电机7驱动端固定连接。U型底板101上表面靠近注射机构6的一侧固定有第二轨道105,注射机构6底端固定有支撑杆106,且支撑杆 106底端与第二轨道105滑动连接。注塑通道9两端分别与型腔8和注射机构6连通。As shown in FIG. 2 and FIG. 3 , the
如图4所示,冷却机构5包括储液箱51和循环泵52,且储液箱51内部设有冷却液,储液箱51的进液口与循环泵52出液口分别连接有第一连接管53和第二连接管54,第一连接管53和第二连接管54另一端分别与冷却通道11两端连通,储液箱51出液口与循环泵52进液口连通。储液箱51内部设有制冷器。冷却通道11为蛇形的弯曲通道。As shown in FIG. 4 , the cooling mechanism 5 includes a
使用时:首先在第一定模2内的型腔8中放入需要镶嵌的尾灯罩原料,接着通过液压机12带动动模4向第一定模2移动完成合模,随后第一定模2所连接的注射机构6开始注射物料,物料从注塑通道9进入型腔8,同时第一定模2内的电加热板10处于加热状态,使得进入第一定模2内的物料保持高温融化状态,当注塑完成后,电加热板10停止加热,液压机12带动动模4与第一定模2脱离,随后伺服电机7带动丝杆104转动,使得两个滑块103会带动第一定模2和第二定模3在滑轨结构1上方移动,从而使得第二定模3与动模4正对,同时第一定模2上的循环泵52开始将储液箱51内的冷却液泵入冷却通道11内对第一定模2进行冷却,帮助产品冷却脱模,在等待第一定模2上的产品进行冷却脱模时,就可以在第二定模3的型腔8中放入新的尾灯罩原料,使得动模4 再与第二定模3合模,第二定模3的注塑操作与第一定模2相同,当第二定模3内的产品完成注塑后,伺服电机7反转,再使得第一定模2与动模4正对,由此往复操作,实现连续注塑。When using: first put the raw material of the tail lamp cover to be inlaid into the cavity 8 in the first
以上所述仅为本实用新型的较佳实施例,并不用以限制本实用新型,凡在本实用新型的精神和原则之内,所作的任何修改、等同替换、改进等,均应包含在本实用新型的保护范围之内。The above are only preferred embodiments of the present invention, and are not intended to limit the present invention. Any modifications, equivalent replacements, improvements, etc. made within the spirit and principles of the present invention shall be included in the present invention. within the scope of protection of the utility model.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122741165.2U CN216329906U (en) | 2021-11-10 | 2021-11-10 | A kind of insert injection molding device of automobile tail lamp mask |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122741165.2U CN216329906U (en) | 2021-11-10 | 2021-11-10 | A kind of insert injection molding device of automobile tail lamp mask |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN216329906U true CN216329906U (en) | 2022-04-19 |
Family
ID=81136626
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202122741165.2U Active CN216329906U (en) | 2021-11-10 | 2021-11-10 | A kind of insert injection molding device of automobile tail lamp mask |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN216329906U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118720065A (en) * | 2024-07-24 | 2024-10-01 | 河北三工耐磨管件制造有限公司 | A precision casting device for double-layer bent pipe castings |
-
2021
- 2021-11-10 CN CN202122741165.2U patent/CN216329906U/en active Active
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118720065A (en) * | 2024-07-24 | 2024-10-01 | 河北三工耐磨管件制造有限公司 | A precision casting device for double-layer bent pipe castings |
| CN118720065B (en) * | 2024-07-24 | 2025-08-12 | 河北三工耐磨管件制造有限公司 | Precise casting device for double-layer bent pipe castings |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN114889058B (en) | Injection port of injection mold | |
| CN215882483U (en) | Injection mold for plastic production | |
| CN219360184U (en) | Automatic water gap cutting structure in mold | |
| CN212045849U (en) | Injection molding integrated robot | |
| CN107901344B (en) | Injection mold capable of rapidly and efficiently demolding and injection molding method thereof | |
| CN207028118U (en) | A kind of injection molded device | |
| CN213321483U (en) | Injection mold capable of achieving rapid demolding | |
| CN210820675U (en) | An injection mold for electric kettle base | |
| CN220995230U (en) | Plastic mold apparatus for producing convenient to drawing of patterns | |
| CN215703601U (en) | Totally enclosed water pump impeller injection mold | |
| CN219114645U (en) | Pen cap forming and processing die | |
| CN210733121U (en) | Laminated mold capable of achieving precise injection molding | |
| CN209504763U (en) | Automobile handle accessory molding die | |
| CN221022205U (en) | Auxiliary in-mold cover closing mold | |
| CN223314346U (en) | Mould structure convenient to open and shut | |
| CN223545707U (en) | A molding die for quick demolding of plastic products | |
| CN219522890U (en) | Injection mold for automobile headlight cover | |
| CN219820500U (en) | Large car back door decorative panel injection molding mold | |
| CN219381444U (en) | Injection mold | |
| CN218196792U (en) | Novel cooling device for injection molding of mold | |
| CN221892516U (en) | Auxiliary injection molding equipment for automobile grille | |
| CN222096860U (en) | High-precision injection mold | |
| CN214324071U (en) | Plastic product processing mold with high heat dissipation and easy demolding | |
| CN211054294U (en) | Injection mold | |
| CN214239427U (en) | An injection mold for the production of PE pipe joints |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |