Disclosure of Invention
The slip form construction method aims at solving the problems that the roundness and the verticality of the cylinder structure are difficult to control in the existing slip form construction of the large-volume cylinder structure, and the construction quality, the safe and stable operation and the use function in the subsequent cylinder of the cylinder structure are influenced. The utility model aims at providing a central drawing disk device of slipform construction.
The utility model provides a technical scheme that its technical problem adopted is: a central drawing plate device for slip form construction comprises:
the central disc is arranged on the inner side of the hydraulic sliding mode device, and the axis of the central disc is overlapped with that of the hydraulic sliding mode device;
and a plurality of pull rods with equal length are arranged along the axial direction of the hydraulic slip form device, one end of each pull rod is connected with the central disc, and the other end of each pull rod is connected to the inner side of the hydraulic slip form device.
The utility model discloses a central drawing plate device of slip form construction, including setting up in the central disc of hydraulic pressure slip form device center, and connect a plurality of pull rods between central disc and hydraulic pressure slip form device, after the pull rod is taut, central drawing plate device forms an organic whole with hydraulic pressure slip form device to utilize whole stretch-draw to carry out effective control to the whole circularity of barrel structure; along with the integral sliding of the hydraulic sliding mode device, the roundness and the verticality of the cylinder structure are judged according to the fastening degree of the pull rod, when the pull rod is loosened, the deviation of the roundness and the verticality of the area of the cylinder structure is shown, and the correction is carried out by adjusting the fastening degree of the pull rod, so that the roundness and the verticality of the whole cylinder structure are controlled; consequently, from installation hydraulic pressure slipform device to accomplishing the slipform construction, utilize the utility model discloses a central drawing dish device can the whole circularity and the straightness that hangs down of overall process dynamic adjustment control tube structure to accomplish along with rectifying in the work progress, guaranteed tube structure's whole circularity and straightness that hangs down, improved tube structure's construction quality, thereby guaranteed tube structure's the safe and stable operation and the service function of follow-up section of thick bamboo interior equipment.
Furthermore, the central disc is annular, a through hole in the center of the central disc is used for connecting pull rods, and the pull rods are symmetrically arranged along the diameter direction of the central disc.
Furthermore, one end of the pull rod, which is close to the central disc, is provided with a right-angled elbow, the right-angled elbow of the pull rod is buckled with the through hole, the intersecting part of the pull rod and the central disc is welded and connected, the other end of the pull rod is provided with a pull ring, and the pull ring is detachably connected with the hydraulic sliding mode device through a connecting assembly.
Furthermore, the connecting assembly comprises a turn buckle and a slip form frame support, one end of the slip form frame support is connected with the upright post bolt of the hydraulic slip form device frame, one end of the turn buckle is connected with the slip form frame support through the bolt, and a lifting hook at the other end of the turn buckle is buckled on the pull ring of the pull rod.
Furthermore, the slipform frame support is provided with a long hole along the length direction, and at least two bolts penetrate through the long hole of the slipform frame support to be in threaded connection with the upright post of the frame body.
Furthermore, the central disc pulling device further comprises a hanging ring in a shape like a Chinese character 'ji', two ends of the hanging ring are buckled in the through hole of the central disc, and the crossing part of the hanging ring and the central disc is connected in a welding mode.
Detailed Description
The present invention will be described in further detail with reference to the following drawings and specific embodiments. It should be noted that the drawings are in simplified form and are not to precise scale, and are provided for convenience and clarity in order to facilitate the description of the embodiments of the present invention.
After the bottom foundation construction of the tubular structure of this embodiment is accomplished, take one's place hydraulic pressure slipform device installation, as shown in fig. 3, install the central drawing set device of slipform construction in hydraulic pressure slipform device inboard, the following description in connection with fig. 1 to fig. 3 the utility model discloses a central drawing set device of slipform construction, it includes:
the central plate 21 is arranged on the inner side of the hydraulic sliding mode device, and the central plate 21 and the axis of the hydraulic sliding mode device are overlapped;
a plurality of tie rods 24 with equal length are arranged along the axial direction of the hydraulic slip form device, one end of the tie rod 24 is connected with the central plate 21, and the other end of the tie rod 24 is connected with the inner side of the hydraulic slip form device.
The utility model discloses a central drawing plate device of slip form construction, including set up in the central disc 21 of hydraulic pressure slip form device center, and connect a plurality of pull rods 24 between central disc 21 and hydraulic pressure slip form device, after pull rod 24 is taut, central drawing plate device and hydraulic pressure slip form device form a whole, thereby utilize whole stretch-draw to carry out effective control to the whole circularity of barrel structure; along with the integral sliding of the hydraulic sliding mode device, the roundness and the verticality of the cylinder structure are judged according to the fastening degree of the pull rod 24, when the pull rod 24 is loosened, the deviation of the roundness and the verticality of the area of the cylinder structure is shown, and the correction is carried out by adjusting the fastening degree of the pull rod 24, so that the roundness and the verticality of the whole cylinder structure are controlled; consequently, from installation hydraulic pressure slipform device to accomplishing the slipform construction, utilize the utility model discloses a central drawing dish device can the whole circularity and the straightness that hangs down of overall process dynamic adjustment control tube structure to accomplish along with rectifying in the work progress, guaranteed tube structure's whole circularity and straightness that hangs down, improved tube structure's construction quality, thereby guaranteed tube structure's the safe and stable operation and the service function of follow-up section of thick bamboo interior equipment.
As shown in FIG. 1, the central disk 21 is ring-shaped, and the through hole at the center of the central disk 21 is used for connecting the pull rod 24, in this embodiment, the central disk 21 is made of Q235B steel with a thickness of 16mm, and has an outer diameter of 1200mm and an inner diameter of 600 mm. The pull rods 24 are symmetrically arranged along the diameter direction of the central disc 21, so that the stress of the whole central disc pulling device is more balanced, the pull rods 24 in the embodiment are made of phi 14 steel bars, and one pull rod 24 is tensioned on each frame body 10 of the hydraulic slip form device. Furthermore, one end of the pull rod 24 close to the central disc 21 is provided with a right-angled bend 241, the right-angled bend 241 of the pull rod 24 is buckled in the through hole, the intersecting part of the pull rod 24 and the central disc 21 is in full-welding connection, the other end of the pull rod 24 is provided with a pull ring, and the pull ring is detachably connected with the hydraulic sliding mode device through a connecting assembly, so that the quick assembly and disassembly of the central disc pulling device are facilitated.
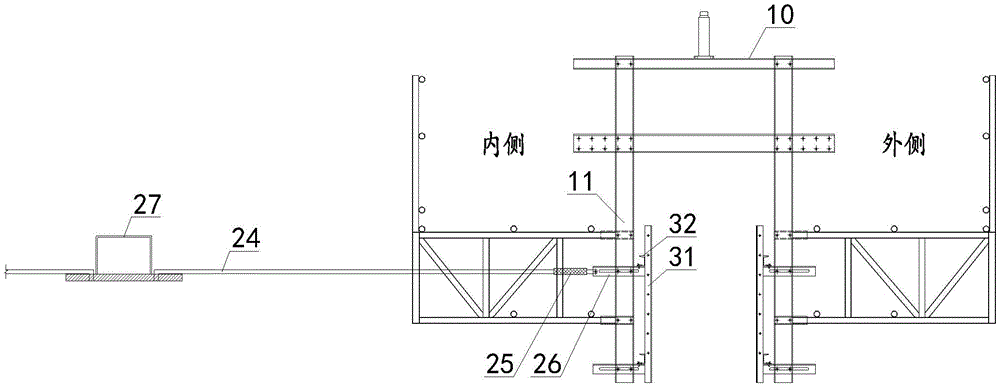
As shown in fig. 2, the connecting assembly includes a turn buckle 25 and a slip form frame support 26, one end of the slip form frame support 26 is connected to the upright post 11 of the hydraulic slip form device frame 10 by a bolt, one end of the turn buckle is connected to the slip form frame support 26 by a bolt, a hook at the other end of the turn buckle is fastened to a pull ring of the pull rod 24, the fastening degree of each pull rod 24 is indirectly adjusted by adjusting the telescopic length of the turn buckle 25, and the purpose of controlling the roundness and verticality of the cylinder structure is further achieved.
As shown in fig. 3, the slipform body support 26 is provided with a long hole 261 along the length direction thereof, two bolts are inserted through the long hole 261 of the slipform body support 26 to be screwed with the upright post 11 of the body 10, and the long hole 261 is provided to facilitate fine adjustment of the horizontal fixing position of the pull rod 24. In order to further enhance the connection strength of the slipform frame brackets 26 and the hydraulic slipform device, the end portions of the slipform frame brackets 26 are welded to the purlin 32 of the formwork device, thereby ensuring stable connection between the central tray pulling device and the hydraulic slipform device.
As shown in fig. 2, the central pull plate device further comprises a hanging ring 27 in a shape like a Chinese character 'ji', two ends of the hanging ring 27 are fastened in the through hole of the central plate 21, the crossed part of the hanging ring 27 and the central plate 21 is in full-welded connection, and the arrangement of the hanging ring 27 provides a hanging point for the subsequent high-altitude removal of the central pull plate device, so that the construction requirement for the removal of the central pull plate device is met.
The use method of the central tray pulling device for slip form construction is described with reference to fig. 1 to 3, and the specific steps are as follows:
after the hydraulic slip form device is installed in place, the central pull disc device is installed on the inner side of the hydraulic slip form device, the axis of the central disc 21 is overlapped with the axis of the hydraulic slip form device, a plurality of pull rods 24 with equal length are radially arranged along the axis of the hydraulic slip form device, one end of each pull rod 24 is connected with the central disc 21, and the other end of each pull rod 24 is connected to the inner side of the hydraulic slip form device; in the sliding and lifting process of the hydraulic sliding mode device, when the pull rod 24 is loosened, the deviation of the whole roundness and the verticality of the area of the cylinder structure is shown, and the fastening degree of the pull rod 24 is adjusted for correction so as to control the whole roundness and the verticality of the whole cylinder structure; after the slip form construction is completed, the whole central pull disc device is hoisted by using mechanical hoisting equipment, the connection between the pull rod 24 and the hydraulic slip form device is loosened, and the central pull disc device is hoisted to the ground on the inner side of the cylinder structure for dismantling.
In summary, firstly, the central disc pulling device is installed in the center of the inner side of the hydraulic slip form device, the axes of the central disc 21 and the hydraulic slip form device are overlapped, one end of the pull rod 24 is connected with the central disc 21, the other end of the pull rod 24 is connected with the inner side of the hydraulic slip form device, and after the pull rod 24 is tensioned, the central disc pulling device and the hydraulic slip form device form a whole, so that the whole roundness of the cylinder structure is effectively controlled by integral tensioning; from installation of the hydraulic sliding form device to completion of sliding form construction, the roundness and perpendicularity of the cylinder structure are judged through the fastening degree of the pull rod 24, the roundness of the cylinder structure is dynamically adjusted and controlled through the central pull disc device, the roundness and perpendicularity of the cylinder structure are effectively controlled, the roundness and perpendicularity of the cylinder structure are guaranteed, the cylinder construction quality is improved, safe and stable operation of the cylinder structure and subsequent in-cylinder equipment use functions are met, and the method has popularization significance particularly for sliding form construction of large-size cylinder structures.
The steps further comprise the steps that after the central drawing disc device is installed, the turn buckle 25 is screwed to be 80% of the tensile load of the turn buckle, after the foundation section of the cylinder structure is poured and before the hydraulic slip form device slides up, the turn buckle 25 is screwed to be 100% of the tensile load of the turn buckle to form complete tensioning, and the integral roundness of the cylinder structure before slip form construction is guaranteed.
The above description is only for the purpose of describing the preferred embodiments of the present invention, and is not intended to limit the scope of the present invention, so that any changes and modifications made by those skilled in the art according to the above disclosure are all within the scope of the appended claims.