CN211386578U - One-step completed inner buckle bending die - Google Patents
One-step completed inner buckle bending die Download PDFInfo
- Publication number
- CN211386578U CN211386578U CN201921306079.5U CN201921306079U CN211386578U CN 211386578 U CN211386578 U CN 211386578U CN 201921306079 U CN201921306079 U CN 201921306079U CN 211386578 U CN211386578 U CN 211386578U
- Authority
- CN
- China
- Prior art keywords
- plate
- die
- bending
- fixing plate
- die assembly
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images

Landscapes
- Bending Of Plates, Rods, And Pipes (AREA)
Abstract
本实用新型提供一种一步完成内扣折弯模具,包括上模组件和下模组件,其特征在于,上模组件包括上模座、上垫板、上固定板和卸料板,上模座、上垫板、上固定板和卸料板从上到下依次固定,成为随压力机能够及时运动的上半段,卸料板;卸料板与上模座、上垫板、上固定板之间安装有矩形弹簧,使两者之间产生相对运动,上固定板靠近下模组件的一侧安装有驱动块,卸料板靠近下模组件的一侧安装有折弯凸模;下模组件位于上模组件的正下方,下模组件从上到下包括:下模板、下固定板、下垫板和下模座,下模板、下固定板、下垫板和下模座之间固定安装。本实用新型生产效率高,工艺简单,成本低的内扣折弯卷圆件冲压模具。
The utility model provides a one-step inner buckle bending die, which includes an upper die assembly and a lower die assembly. The upper die seat, the upper backing plate, the upper fixing plate and the discharge plate are fixed in sequence from top to bottom, and become the upper half section that can move in time with the press, the discharging plate; A rectangular spring is installed between the upper fixing plates to cause relative movement between the two. A drive block is installed on the side of the upper fixing plate close to the lower die assembly, and a bending plate is installed on the side of the stripper plate close to the lower die assembly. Punch; the lower die assembly is located just below the upper die assembly, the lower die assembly from top to bottom includes: lower template, lower fixing plate, lower pad and lower die base, lower template, lower fixing plate, lower pad Fixed installation between the plate and the lower die base. The utility model has the advantages of high production efficiency, simple process and low cost, and is a stamping die for an inner buckle, bending and rolling round piece.
Description
技术领域technical field
本实用新型主要涉及冲压模具领域,尤其涉及一种一步完成内扣折弯模具。The utility model mainly relates to the field of stamping die, in particular to a one-step inner buckle bending die.
背景技术Background technique
在冲压加工行业中,经常会遇到类似卷圆零件,传统的做法是需要多步成型后才可以完成卷圆的工序,工序繁杂,费时费力,效率低,成本高。In the stamping processing industry, similar rounded parts are often encountered. The traditional method is to complete the rounding process after multi-step forming. The process is complicated, time-consuming, labor-intensive, low-efficiency and high-cost.
已公开中国发明专利,申请号CN201711134539.6,专利名称:一种折弯冲压模具,申请日:2017-11-16,本实用新型涉及一种折弯冲压模具,包括上模座、下模座、固定上夹板、折弯冲头、折弯模具平台、气缸、伸缩导柱和固定导套,所述上模座的底部中间设有折弯冲头,所述上模座的底部设有固定上夹板,且所述上模座与固定上夹板的大小一致,所述固定上夹板的中间设有导向孔,所述导向孔与折弯冲头为对应结构,所述固定上夹板的底部设有下模座,所述下模座的顶部设有折弯模具平台,所述下模座的底部两侧设有气缸,所述下模座的顶部两侧分布有伸缩导柱。该折弯冲压模具,通过在下模座的底部两侧均设置气缸,且在气缸的顶部设置三个伸缩导柱,便于固定上夹板升降进行折弯冲压模具工作,可有效的控制上模座,使其在工作时带动折弯冲头进行折弯。Chinese invention patent has been published, application number CN201711134539.6, patent name: a bending stamping die, application date: 2017-11-16, the utility model relates to a bending stamping die, comprising an upper die seat and a lower die seat , Fix the upper splint, the bending punch, the bending die platform, the cylinder, the telescopic guide post and the fixed guide sleeve. The upper splint, and the size of the upper die base and the fixed upper splint is the same, the middle of the fixed upper splint is provided with a guide hole, the guide hole and the bending punch are corresponding structures, and the bottom of the fixed upper splint is provided with a guide hole. There is a lower die base, a bending die platform is arranged on the top of the lower die base, cylinders are arranged on both sides of the bottom of the lower die base, and telescopic guide columns are distributed on both sides of the top of the lower die base. The bending stamping die is provided with air cylinders on both sides of the bottom of the lower die base, and three telescopic guide columns are set on the top of the cylinder, which is convenient for fixing the upper clamp plate to lift and perform the bending stamping die work, and can effectively control the upper die base. Make it drive the bending punch for bending during work.
实用新型内容Utility model content
本实用新型提供一种一步完成内扣折弯模具,针对现有技术的上述缺陷,提供一种一步完成内扣折弯模具,包括上模组件和下模组件,其特征在于,所述上模组件包括上模组件和下模组件,其特征在于,所述上模组件包括上模座1、上垫板2、上固定板3和卸料板4,上模座1、上垫板2、上固定板3和卸料板4从上到下依次固定,成为随压力机能够及时运动的上半段;The utility model provides a one-step inner buckle bending die, aiming at the above-mentioned defects of the prior art, provides a one-step inner buckle bending die, which includes an upper die assembly and a lower die assembly, and is characterized in that the The upper die assembly includes an upper die assembly and a lower die assembly, characterized in that the upper die assembly includes an
所述卸料板4与上模座1、上垫板2、上固定板3之间安装有矩形弹簧A12,使两者之间产生相对运动,所述上固定板3靠近下模组件的一侧安装有驱动块9,所述卸料板4靠近下模组件的一侧安装有折弯凸模13;A rectangular spring A12 is installed between the
所述下模组件位于上模组件的正下方,所述下模组件从上到下包括:下模板5、下固定板6、下垫板7和下模座8,所述下模板5、下固定板6、下垫板7和下模座8之间固定安装;The lower mold assembly is located directly below the upper mold assembly, and the lower mold assembly includes from top to bottom: a
所述下固定板6内置导向板11,所述下模组件内设置有与导向板11相对滑动的安装在有矩形弹簧B15的滑块10上,所述滑块10 设有与驱动块9配合的斜面,The
所述在滑块10靠近折弯凸模13的一侧镶有成型块16,所述下模板5对应折弯凸模13设置有折弯凹模14,所述下模板5还设置有定位制件19的导正销17。The side of the slider 10 close to the
优选的,上模座1、上垫板2、上固定板3和卸料板4之间通过等高螺丝18固定。Preferably, the
优选的,导正销17设置在下模板5靠近制件19的一侧,并穿设过制件19。Preferably, the
优选的,驱动块9靠近滑块10斜面的一侧设置有对应的斜面,所述斜面的上下两边均设置有圆角。Preferably, the side of the
优选的,驱动块9通过螺栓固定安装在上垫板2靠近下模组件的一侧上。Preferably, the
优选的,导向板11通过螺栓固定安装在下垫板7上,所述螺栓设置有多个。Preferably, the
优选的,成型块16的形状与产品形状相对应。Preferably, the shape of the forming
本实用新型的有益效果:通过驱动块及滑块斜面的驱动设置,实现卷圆折弯工序,提高了效率,制件与折弯凸模及折弯凹模脱离后即可取件,降低了模具开发成本,提高工件的稳定性。The beneficial effects of the utility model are as follows: through the drive arrangement of the drive block and the inclined surface of the slider, the rolling and bending process is realized, and the efficiency is improved. Development costs, improve the stability of the workpiece.
附图说明Description of drawings
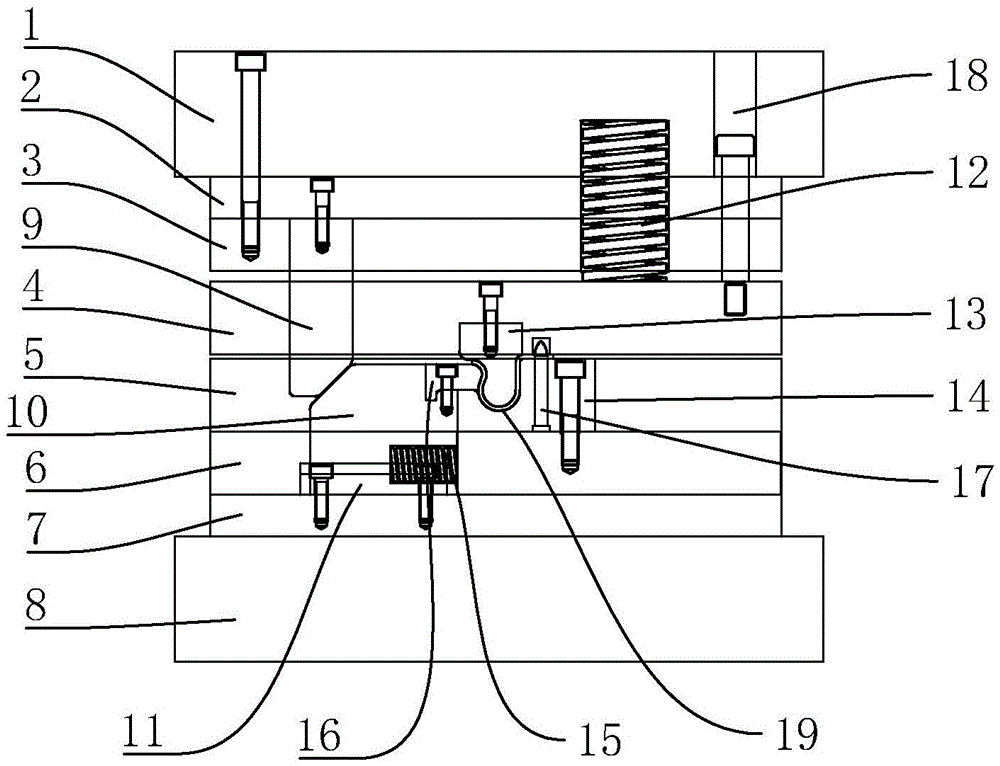
图1为本实用新型的结构图;Fig. 1 is the structural drawing of the utility model;
图中,In the figure,
1、上模座;2、上垫板;3、上固定板;4、卸料板;5、下模板;6、下固定板;7、下垫板;8、下模座;9、驱动块;10、滑块;11、导向板;12、矩形弹簧A;13、折弯凸模;14、折弯凹模;15、矩形弹簧B;16、成型块;17、导正销;18、等高螺丝;19、制件。1. Upper die base; 2. Upper backing plate; 3. Upper fixing plate; 4. Stripping plate; 5. Lower die plate; 6. Lower fixing plate; 7. Lower backing plate; 8. Lower die holder; 9. Drive block; 10, slider; 11, guide plate; 12, rectangular spring A; 13, bending punch; 14, bending die; 15, rectangular spring B; 16, forming block; 17, guide pin; 18 , Contour screws; 19. Parts.
具体实施方式Detailed ways
如图1所示可知,本实用新型包括有:上模组件和下模组件,其特征在于,所述上模组件包括上模座1、上垫板2、上固定板3和卸料板4,上模座1、上垫板2、上固定板3和卸料板4从上到下依次固定,成为随压力机能够及时运动的上半段;As shown in FIG. 1, the utility model includes: an upper die assembly and a lower die assembly, characterized in that the upper die assembly includes an
所述卸料板4与上模座1、上垫板2、上固定板3之间安装有矩形弹簧A12,使两者之间产生相对运动,所述上固定板3靠近下模组件的一侧安装有驱动块9,所述卸料板4靠近下模组件的一侧安装有折弯凸模13;A rectangular spring A12 is installed between the
所述下模组件位于上模组件的正下方,所述下模组件从上到下包括:下模板5、下固定板6、下垫板7和下模座8,所述下模板5、下固定板6、下垫板7和下模座8之间固定安装;The lower mold assembly is located directly below the upper mold assembly, and the lower mold assembly includes from top to bottom: a
所述下固定板6内置导向板11,所述下模组件内设置有与导向板11相对滑动的安装在有矩形弹簧B15的滑块10上,所述滑块10 设有与驱动块9配合的斜面,The
所述在滑块10靠近折弯凸模13的一侧镶有成型块16,所述下模板5对应折弯凸模13设置有折弯凹模14,所述下模板5还设置有定位制件19的导正销17。The side of the slider 10 close to the
在使用中,包括以下步骤:In use, the following steps are included:
第一步:冲床工作:Step 1: Punch work:
上模座1、上垫板2、上固定板3、卸料板4连接的全部原件矩形弹簧A12,驱动块9,折弯凹模13开始下行,折弯凹模13先接触制件19,导正钉17插入制件19中,在继续下行的过程中,折弯凸模13开始对制件19施加一定的作用力,此时卸料板4,折弯凸模13 停止下行,All the original rectangular springs A12 connected with the
由于上模座1、上垫板2、上固定板3与卸料板4为弹性连接,上模座1继续下行,驱动块9也继续随上模座1继续下行,驱动块9 下端斜面接触到滑块10的上端斜面,滑块10在斜面驱动的侧向作用力下,滑块10的移动由导向板11导向,当上模下行至机床的下死点时,制件19移动至折弯凸模13,折弯凹模14的对应部分的贴紧的位置,一步完成内扣折弯冲压成型.Since the
第二步:冲压作业后完成:Step 2: Finished after stamping operation:
冲床滑块开始向上运动,上模座1、上垫板2、上固定板3也开始往上运动,驱动块9向上运动,折弯凸模13和卸料板4先保持不动,在上行的过程中,驱动块9下端斜面与滑块10的斜面逐渐分离,滑块10和成型块16在矩形弹簧B15的作用下复位,这时折弯凸模 13和折弯凹模14完全分离,卸料板4继续上行,回到模具的上死点,此时即可取件.The slider of the punch press starts to move upward, the
在本实施中优选的,上模座1、上垫板2、上固定板3和卸料板 4之间通过等高螺丝18固定。In this implementation, preferably, the
设置上述结构,起到在工作时整体上模组件的稳定性。The above structure is provided to provide stability of the mold assembly as a whole during operation.
在本实施中优选的,导正销17设置在下模板5靠近制件19的一侧,并穿设过制件19。In this embodiment, preferably, the
设置上述结构,折弯首步骤就是将制件19放入导正销17,起到定位作用。With the above-mentioned structure, the first step of bending is to put the
在本实施中优选的,驱动块9靠近滑块10斜面的一侧设置有对应的斜面,所述斜面的上下两边均设置有圆角。In this embodiment, preferably, the side of the driving
设置上述结构,防止在工作过程中起到摩擦作用,一定的圆滑性,保证工具的使用时间,降低返修率。The above structure is provided to prevent friction in the working process, and a certain smoothness can ensure the use time of the tool and reduce the repair rate.
在本实施中优选的,驱动块9通过螺栓固定安装在上垫板2靠近下模组件的一侧上。In this embodiment, preferably, the driving
设置上述结构,通过螺栓的使用,保证驱动块9安装固定的稳定性,提高使用时的稳定性。The above structure is provided, and the stability of the installation and fixation of the driving
在本实施中优选的,导向板11通过螺栓固定安装在下垫板7上,所述螺栓设置有多个。In this embodiment, preferably, the
设置上述结构,通过螺栓的使用,保证导向板11安装固定的稳定性,提高使用时的稳定性。With the above structure, the use of bolts ensures the stability of the installation and fixation of the
在本实施中优选的,成型块16的形状与产品形状相对应。Preferably in this embodiment, the shape of the forming
设置上述结构,不局限成型块16的形状,起到灵活运用的作用,提高产品的使用率。The above structure is provided, the shape of the forming
上述实施例仅例示性说明本专利申请的原理及其功效,而非用于限制本专利申请。任何熟悉此技术的人士皆可在不违背本专利申请的精神及范畴下,对上述实施例进行修饰或改变。因此,举凡所属技术领域中具有通常知识者在未脱离本专利申请所揭示的精神与技术思想下所完成的一切等效修饰或改变,仍应由本专利请的权利要求所涵盖。The above-mentioned embodiments merely illustrate the principles and effects of the present patent application, but are not intended to limit the present patent application. Anyone skilled in the art can make modifications or changes to the above embodiments without departing from the spirit and scope of the present patent application. Therefore, all equivalent modifications or changes made by those with ordinary knowledge in the technical field without departing from the spirit and technical idea disclosed in this patent application shall still be covered by the claims of this patent application.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921306079.5U CN211386578U (en) | 2019-08-13 | 2019-08-13 | One-step completed inner buckle bending die |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921306079.5U CN211386578U (en) | 2019-08-13 | 2019-08-13 | One-step completed inner buckle bending die |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211386578U true CN211386578U (en) | 2020-09-01 |
Family
ID=72229801
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921306079.5U Expired - Fee Related CN211386578U (en) | 2019-08-13 | 2019-08-13 | One-step completed inner buckle bending die |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211386578U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112872137A (en) * | 2021-01-08 | 2021-06-01 | 深圳市亿和精密科技集团有限公司 | Buckling and bending forming device for upper cross beam of automobile seat |
| CN113145696A (en) * | 2021-04-14 | 2021-07-23 | 中山数码模汽车技术有限公司 | Multi-bending inner buckle forming structure and method for automobile seat side plate part |
| CN114433725A (en) * | 2020-10-30 | 2022-05-06 | 青岛海信模具有限公司 | Bending die |
| CN115780651A (en) * | 2022-11-25 | 2023-03-14 | 江西江铃底盘股份有限公司 | Bending-bending composite die for negative-angle special-shaped wire harness support of electrically driven rear axle of automobile and composite machining process of bending-bending composite die |
-
2019
- 2019-08-13 CN CN201921306079.5U patent/CN211386578U/en not_active Expired - Fee Related
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114433725A (en) * | 2020-10-30 | 2022-05-06 | 青岛海信模具有限公司 | Bending die |
| CN114433725B (en) * | 2020-10-30 | 2024-03-12 | 青岛海信模具有限公司 | Bending die |
| CN112872137A (en) * | 2021-01-08 | 2021-06-01 | 深圳市亿和精密科技集团有限公司 | Buckling and bending forming device for upper cross beam of automobile seat |
| CN112872137B (en) * | 2021-01-08 | 2022-10-21 | 深圳市亿和精密科技集团有限公司 | Buckling and bending forming device for upper cross beam of automobile seat |
| CN113145696A (en) * | 2021-04-14 | 2021-07-23 | 中山数码模汽车技术有限公司 | Multi-bending inner buckle forming structure and method for automobile seat side plate part |
| CN115780651A (en) * | 2022-11-25 | 2023-03-14 | 江西江铃底盘股份有限公司 | Bending-bending composite die for negative-angle special-shaped wire harness support of electrically driven rear axle of automobile and composite machining process of bending-bending composite die |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN206716847U (en) | A kind of flange punching die | |
| CN103785754A (en) | Cold stamping drawing die | |
| CN204182800U (en) | A kind of compound punching structure for punch level progressive die | |
| CN205926794U (en) | Punching composite die | |
| CN211386579U (en) | Stamping die capable of bending up and down in one step | |
| CN211386580U (en) | Negative angle shaping mould structure of bending | |
| CN202984359U (en) | Pre-ejecting-type sheet metal part bending forming device | |
| CN119549570B (en) | Sheet metal stamping forming equipment for trowelling machine shell processing | |
| CN201799525U (en) | Die with tapered wedge | |
| CN208050743U (en) | A kind of rollover holes mechanism of diel | |
| CN205798168U (en) | For processing the bending die of Z-shaped support | |
| CN222790377U (en) | Automobile mould with time-delay mechanism | |
| CN213052198U (en) | Thick plate bending forming die | |
| CN202174164U (en) | Multifunctional one-step forming die | |
| CN201969806U (en) | Bending flap demoulding mechanism | |
| CN219130515U (en) | Sliding block stripping mechanism | |
| CN115041593B (en) | Forming die and forming process for lower supporting plate of middle channel of automobile | |
| CN216137898U (en) | Bending die | |
| CN202803916U (en) | Cold punching compound mould | |
| CN211916010U (en) | Oblique Comb Guide Roll Riveting Equipment | |
| CN208019269U (en) | A kind of seesaw mould structure | |
| CN209631942U (en) | An Improved Stamping Die | |
| CN113198910A (en) | Mould of quick control location nail lift in mould | |
| CN216461057U (en) | Side flanging die stripping mechanism | |
| CN223043461U (en) | Bending and riveting machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20200901 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |