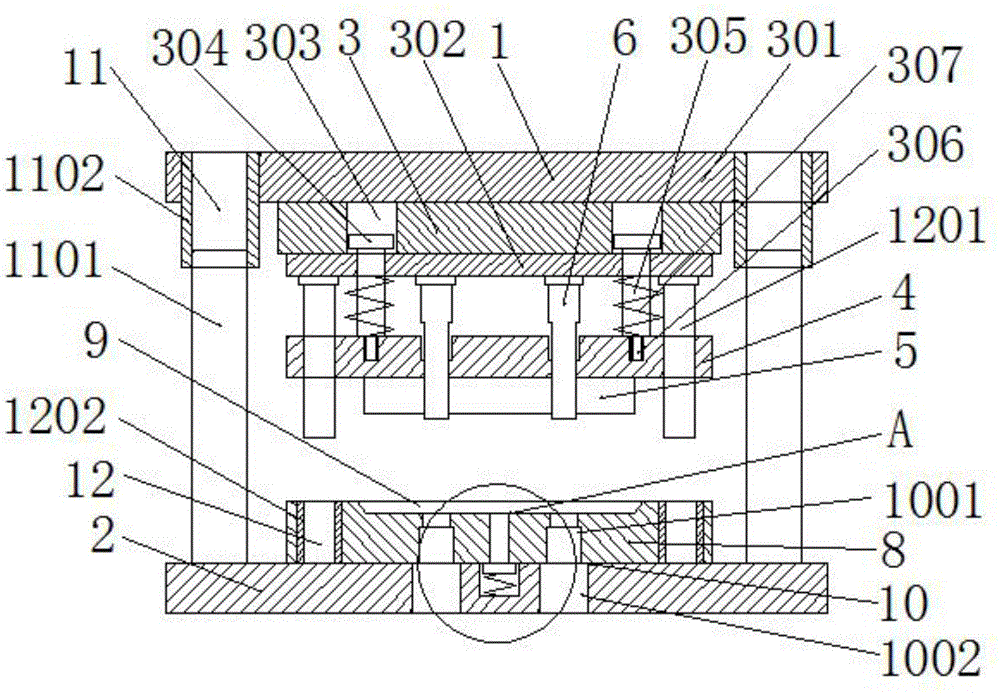
Low-carbon-ring automobile side cross beam forming die
Technical Field
The utility model relates to an automotive production field specifically is low carbon environmental protection car side crossbeam forming die.
Background
The cross member of the automobile is used for ensuring the torsional rigidity of the automobile frame and bearing longitudinal load, and can also support main components on the automobile. Typically, trucks have 5-6 beams, sometimes more. The structure of the edge beam type frame is characterized in that the frame is convenient for installing a cab, a carriage and some special equipment and arranging other assemblies, and is beneficial to refitting modified vehicles and developing various vehicles, so that the frame is widely applied to cargo vehicles and most special vehicles. The automobile side cross beam is mainly formed by cold stamping, so that a low-carbon ring automobile side cross beam forming die is needed.
Part of cold stamping dies for automobile side beams are inconvenient to demold, and after stamping is completed, a formed part is attached to a core or a cavity at a certain probability and is inconvenient to demold; part car side beam cold stamping die can't realize punching a hole and bending simultaneously, punches a hole and bends and fall into two processes processing, and not only inefficiency produces positioning error easily moreover, is unfavorable for product quality's improvement.
SUMMERY OF THE UTILITY MODEL
An object of the utility model is to provide a low carbon environmental protection car side crossbeam forming die sets up demoulding mechanism and lower demoulding mechanism, can be ejecting with the car side crossbeam after the shaping, and the drawing of patterns of being convenient for sets up drift and core, can accomplish simultaneously and punch a hole and bend two processes, improves production efficiency to solve the problem that proposes in the above-mentioned background art.
In order to achieve the above object, the utility model provides a following technical scheme: low carbon ring guarantor car side crossbeam forming die, including upper die base and die holder, the upper die base downside passes through demoulding mechanism on the bolt fixedly connected with, go up demoulding mechanism downside fixedly connected with terrace die, terrace die downside fixedly connected with core, go up demoulding mechanism downside fixedly connected with drift, the drift runs through terrace die and core, demoulding mechanism under the die holder upside fixedly connected with, the die holder upside passes through screw fixedly connected with die, the die cavity has been seted up to the die upside, blanking mechanism has been seted up on die holder and the die, be provided with first guiding mechanism on die holder and the upper die base, it is provided with second guiding mechanism to go up demoulding mechanism downside.
Preferably, the upper demoulding mechanism comprises a first fixing plate, the upper side of the first fixing plate is fixedly connected with the upper die base, and the lower side of the first fixing plate is fixedly connected with a second fixing plate (302) through a screw.
Preferably, four groups of first through holes are formed in the first fixing plate, limiting blocks are arranged in the four groups of first through holes, and the outer surfaces of the four groups of limiting blocks are respectively connected to the four groups of first through holes in a sliding mode.
Preferably, the lower sides of the four groups of limiting blocks are fixedly welded with connecting columns, one ends of the four groups of connecting columns penetrate through the second fixing plate, threaded columns are fixedly welded at the lower ends of the four groups of connecting columns, and the surfaces of the threaded columns are in threaded connection with the male die.
Preferably, the outer surface of the connecting column is sleeved with a first spring in a sliding manner, and two ends of the first spring are respectively attached to the second fixing plate and the male die.
Preferably, lower demoulding mechanism includes the second through-hole, the second through-hole sets up inside the die holder, the inside second spring that is provided with of second through-hole, second spring upside is provided with the ladder post, the die is run through to ladder post upper end, the ladder post tip extends in the die cavity.
Preferably, the first guide mechanism comprises a first guide pillar, the lower end of the first guide pillar is fixedly connected to the upper side of the lower die holder, a first guide sleeve is connected to the outer surface of the first guide pillar in a sliding mode, and the outer surface of the first guide sleeve is fixedly inserted into the upper die holder.
Preferably, the second guide mechanism comprises a second guide pillar, the upper end of the second guide pillar is fixedly connected to the lower side of the second fixing plate, one end of the second guide pillar penetrates through the male die, a second guide sleeve is connected to the surface of the second guide pillar in a sliding mode, and the outer surface of the second guide sleeve is fixedly inserted into the female die.
Preferably, the blanking mechanism comprises a stepped hole, the stepped hole is formed in the female die, the stepped hole is communicated with a blanking hole, and the blanking hole is formed in the lower die holder.
Compared with the prior art, the beneficial effects of the utility model are that:
1. the upper demoulding mechanism and the lower demoulding mechanism are arranged, so that the formed car side cross beam can be ejected out, demoulding is facilitated, and the production efficiency is improved;
2. the male die is provided with a punch and a core, and the female die is provided with a corresponding blanking mechanism and a corresponding cavity, so that two processes of punching and bending can be completed simultaneously, and the product precision is improved.
Drawings
FIG. 1 is a schematic view of the internal structure of the present invention;
FIG. 2 is a schematic view of a portion A of FIG. 1 according to the present invention;
fig. 3 is a schematic view of the structure of the concave die part in the top view of the present invention.
In the figure: 1. an upper die holder; 2. a lower die holder; 3. an upper demolding mechanism; 4. a male die; 5. a core; 6. a punch; 7. a lower demolding mechanism; 8. a female die; 9. a cavity; 10. a blanking mechanism; 11. a first guide mechanism; 12. a second guide mechanism; 301. a first fixing plate; 302. a second fixing plate; 303. a first through hole; 304. a limiting block; 305. connecting columns; 306. a threaded post; 307. a first spring; 701. a second through hole; 702. a second spring; 703. a stair post; 1101. a first guide post; 1102. a first guide sleeve; 1201. a second guide post; 1202. a second guide sleeve; 1001. a stepped hole; 1002. and (7) blanking holes.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
Referring to fig. 1-3, the present invention provides a technical solution: low carbon ring guarantor car side crossbeam forming die, including upper die base 1 and die holder 2, for the convenience of drawing of patterns, demoulding mechanism 3 on 1 downside of upper die base through bolt fixedly connected with, upward demoulding mechanism 3 includes first fixed plate 301, and first fixed plate 301 upside fixed connection is in upper die base 1, and first fixed plate 301 downside passes through screw fixedly connected with second fixed plate 302. Four groups of first through holes 303 are formed in the first fixing plate 301, the first through holes 303 can provide a space for the limiting blocks 304 to move up and down, so that the male die 4 can move up and down conveniently, and the formed part can be ejected out, the limiting blocks 304 are arranged in the four groups of first through holes 303, and the outer surfaces of the four groups of limiting blocks 304 are respectively connected to the four groups of first through holes 303 in a sliding mode. The lower sides of the four sets of limiting blocks 304 are fixedly welded with connecting columns 305, one ends of the four sets of connecting columns 305 penetrate through the second fixing plate 302, the lower ends of the four sets of connecting columns 305 are fixedly welded with threaded columns 306, and the surfaces of the four sets of threaded columns 306 are in threaded connection with the male die 4. In order to eject the formed part, a certain force is required to be provided by the spring, so that the first spring 307 is slidably sleeved on the outer surface of the connecting column 305, and two ends of the first spring 307 are respectively attached to the second fixing plate 302 and the male die 4. In the process that the male die 4 is pressed downwards, the core 5 drives the male die 4 to move upwards under the reactive force of the blank until the upper side of the male die 4 is attached to the lower side of the second fixing plate 302, in the process that the male die 4 moves upwards, the connecting column 305 and the limiting block 304 move upwards along the first through hole 303 without blocking the male die 4 to move upwards, the first spring 307 is compressed, after the forming is finished, a punched hole on the car side cross beam is clamped on the punch 6, and the first spring 307 pushes the male die 4 and the core 5 to press downwards, so that the car side cross beam can be ejected out, and the demoulding is finished.
For the convenience of punching and bending simultaneously, 3 downside fixedly connected with terrace dies 4 at last demoulding mechanism, 4 downside fixedly connected with cores 5 of terrace dies, 3 downside fixedly connected with drift 6 of last demoulding mechanism, drift 6 runs through terrace dies 4 and cores 5, for the convenience of drawing of patterns, demoulding mechanism 7 under 2 upside fixedly connected with of die holder, lower demoulding mechanism 7 includes second through-hole 701, second through-hole 701 sets up inside die holder 2, the inside second spring 702 that is provided with of second through-hole 701, second spring 702 upside is provided with ladder post 703, ladder post 703 upper end runs through die 8, ladder post 703 tip extends in die cavity 9. When the core 5 and the punch 6 are pressed down, the stepped column 703 can be compressed into the second through hole 701 without affecting the positive working. In the forming process of the blank, the stepped column 703 is pressed downwards, the second spring 702 is compressed, and when the upper die base 1 moves upwards, the second spring 702 pushes the stepped column 703 to eject the formed vehicle side cross beam upwards.
The die 8 is fixedly connected to the upper side of the lower die holder 2 through a screw, the die cavity 9 is formed in the upper side of the die 8, the blanking mechanism 10 is arranged on the lower die holder 2 and the die 8, the blanking mechanism 10 comprises a stepped hole 1001, the stepped hole 1001 is arranged inside the die 8, the stepped hole 1001 is communicated with a blanking hole 1002, and the blanking hole 1002 is arranged inside the lower die holder 2. The lower die holder 2 and the upper die holder 1 are provided with a first guide mechanism 11, the first guide mechanism 11 comprises a first guide pillar 1101, the lower end of the first guide pillar 1101 is fixedly connected to the upper side of the lower die holder 2, the outer surface of the first guide pillar 1101 is slidably connected with a first guide sleeve 1102, and the outer surface of the first guide sleeve 1102 is fixedly inserted into the upper die holder 1.
A second guide mechanism 12 is provided on the lower side of the upper ejector mechanism 3. The second guiding mechanism 12 includes a second guide pillar 1201, an upper end of the second guide pillar 1201 is fixedly connected to a lower side of the second fixing plate 302, one end of the second guide pillar 1201 penetrates through the male mold 4, a second guide sleeve 1202 is slidably connected to a surface of the second guide pillar 1201, and an outer surface of the second guide sleeve 1202 is fixedly inserted into the female mold 8.
The working principle is as follows: the automobile beam blank is fed onto the female die 8, the upper die holder 1 is driven by a punch to press downwards, the first guide mechanism 11 and the second guide mechanism 12 can prevent the male die 4 and the female die 8 from moving transversely, the punching precision is improved, in the pressing process of the upper die holder 1, the punch 6 firstly contacts the automobile beam blank and can punch a required hole, waste materials are discharged downwards through the blanking mechanism 10, in the punching and pressing process, the core 5 contacts the blank, under the reaction force of the blank, the core 5 drives the male die 4 to move upwards until the upper side of the male die 4 is attached to the lower side of the second fixing plate 302, in the upward moving process of the male die 4, the connecting column 305 and the limiting block 304 move upwards along the first through hole 303 without obstructing the upward movement of the male die 4, the first spring 307 is compressed, the blank 4 is bent and formed in the male die cavity 9 under the pushing of the second fixing plate 302, in the blank forming process, the stepped column 703 is pressed downwards, the second spring 702 is compressed, then the punching machine drives the upper die holder 1 to move upwards, the second spring 702 pushes the stepped column 703 to upwards eject the formed car side cross beam, a punched hole on the car side cross beam is clamped on the punch 6, the first spring 307 pushes the male die 4 and the die core 5 to press downwards, and the car side cross beam can be ejected out, so that the forming is completed.
Although embodiments of the present invention have been shown and described, it will be appreciated by those skilled in the art that changes, modifications, substitutions and alterations can be made in these embodiments without departing from the principles and spirit of the invention, the scope of which is defined in the appended claims and their equivalents.