CN202934376U - A milling machine fixture - Google Patents

A milling machine fixture Download PDF

Info

Publication number
CN202934376U
CN202934376U CN 201220568521 CN201220568521U CN202934376U CN 202934376 U CN202934376 U CN 202934376U CN 201220568521 CN201220568521 CN 201220568521 CN 201220568521 U CN201220568521 U CN 201220568521U CN 202934376 U CN202934376 U CN 202934376U
Authority
CN
China
Prior art keywords
milling machine
workpiece
fixture
bolt
threaded hole
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Expired - Fee Related
Application number
CN 201220568521
Other languages
Chinese (zh)
Inventor
黄财明
孙艳
陈杰
李伟飞
吴海峰
王瑞平
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Zhejiang Geely Holding Group Co Ltd
Zhejiang Geely Power Train Co Ltd
Jinan Geely Auto Parts Co Ltd
Hunan Luoyou Engine Parts Co Ltd
Original Assignee
Zhejiang Geely Holding Group Co Ltd
Zhejiang Geely Luoyou Engine Co Ltd
Jinan Geely Auto Parts Co Ltd
Hunan Luoyou Engine Parts Co Ltd
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by Zhejiang Geely Holding Group Co Ltd, Zhejiang Geely Luoyou Engine Co Ltd, Jinan Geely Auto Parts Co Ltd, Hunan Luoyou Engine Parts Co Ltd filed Critical Zhejiang Geely Holding Group Co Ltd
Priority to CN 201220568521 priority Critical patent/CN202934376U/en
Application granted granted Critical
Publication of CN202934376U publication Critical patent/CN202934376U/en
Anticipated expiration legal-status Critical
Expired - Fee Related legal-status Critical Current

Links

Images

Landscapes

  • Jigs For Machine Tools (AREA)

Abstract

本实用新型公开了一种铣床夹具包括用于和铣床基板连接的T形座以及和T形座螺栓连接的夹具本体,夹具本体的侧面设有贯通的螺纹孔,螺纹孔内设有压紧螺栓,压紧螺栓的头部设有压紧块。工件放在铣床基板上之后只需要在工件周围的铣床基板槽内固定夹具,拧紧压紧螺栓使得压紧块顶紧工件侧面即可加工整个平面,不需要二次装夹和加工。因此,本实用新型具有能保证一次装夹就能铣削加工整个工件平面,从而保证加工精度和加工质量的有益效果。
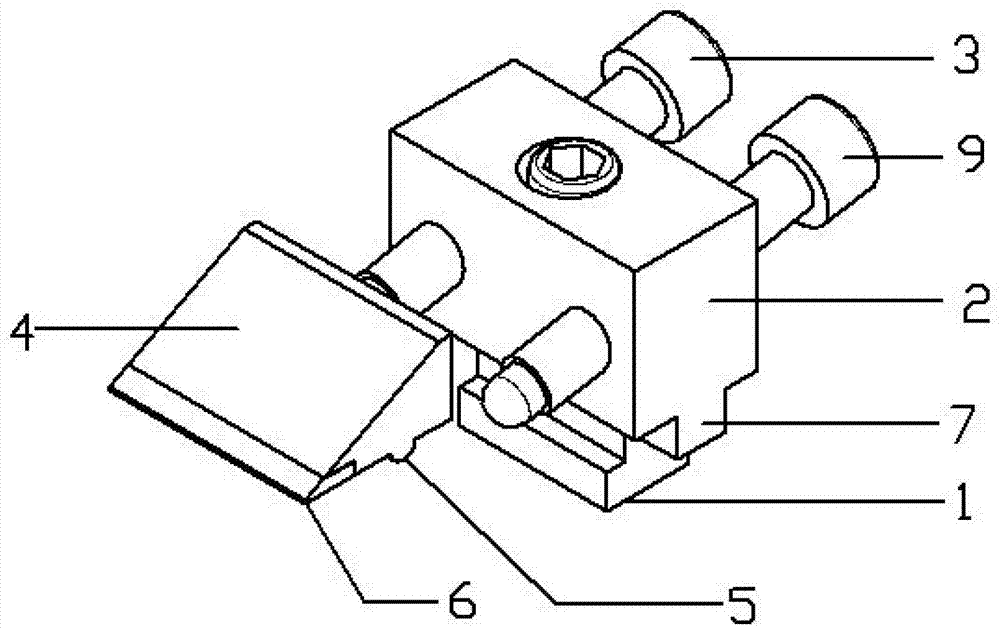
Figure 201220568521

The utility model discloses a milling machine fixture which comprises a T-shaped seat for connecting with a milling machine base plate and a fixture body connected with a bolt of the T-shaped seat. The side of the fixture body is provided with a through threaded hole, and a pressing bolt is arranged in the threaded hole. , the head of the compression bolt is provided with a compression block. After the workpiece is placed on the base plate of the milling machine, it is only necessary to fix the fixture in the groove of the base plate of the milling machine around the workpiece, and tighten the clamping bolt so that the clamping block presses against the side of the workpiece to process the entire plane without secondary clamping and processing. Therefore, the utility model has the beneficial effects of being able to mill and process the entire plane of the workpiece in one clamping, thereby ensuring the processing accuracy and processing quality.

Figure 201220568521

Description

A kind of fraise jig
Technical field
The utility model relates to a kind of fixture, relates in particular to a kind of fraise jig.
Background technology
Planer-type milling machine is broad-spectrum heavy machine tool, and planer-type milling machine machining accuracy and productivity ratio are all higher, is adapted at reaching in batch plane and the inclined-plane of machining large workpiece in production in enormous quantities, is applicable to large-scale sheet metal component or the processing such as casing part and mould.Gantry mill is in the middle of the process of the large plane steel plate of processing, at first for the first time clamping, most of area machine-shaping of steel plate, because common fixture is all the compression type fixture, the position of clamp pressing for the first time can't Milling Process, then by the clamping that replaces for the second time, the position milling of clamp pressing for the first time, the flatness processed through the large plane steel plate of clamping Milling Process moulding for the second time like this is not good, all the step with the tool marks junction exists, and has a strong impact on machining accuracy and crudy.
Chinese patent Granted publication number: CN202399062U, August 29 2012 Granted publication day, a kind of fraise jig group is disclosed, comprise at least two for holding workpiece and be located at the fixture on the substrate of milling machine, fixture comprises positioner, positioner comprises pressing plate and the first support column, and the bottom of the first support column is located on the substrate of milling machine; One end of pressing plate is located on the first support column, and the place, top of workpiece is located in the opposite end of pressing plate; Fixture also comprises at least one vibration absorber of being located on substrate and being resisted against the workpiece bottom.Cutter for milling machines is in processing work when surface, due to the effect of cutting force, and the workpiece vibration-generating, at this moment vibration absorber can absorb the energy of Workpiece vibration, thereby makes the workpiece held stationary.This fixture can be fixed on workpiece on the substrate of milling machine preferably, and vibration absorber is supporting workpiece simultaneously, has reduced the vibration of workpiece in process.Its weak point is that this kind of fixture understood on some machined surface that is pressed in workpiece in clamping, after processing, the position of clamp pressing can't complete Milling Process for the first time, need clamping processing for the second time, easily there is step in surface of the work through twice clamping processing in the tool marks junction, cause that surface of the work is rough, out-of-flatness, have a strong impact on crudy and machining accuracy.
The utility model content
The utility model is pressed on surface of the work the surface that causes workpiece and need to just can completes the processing on whole surface through twice clamping Milling Process in order to overcome fraise jig of the prior art, thereby can produce in the tool clear of work junction deficiency that step has a strong impact on machining accuracy and crudy after twice clamping processing, provide a kind of to need clamped one time just can complete the Milling Process of surface of the work, thereby guaranteed the fraise jig of crudy and machining accuracy.
To achieve these goals, the utility model adopts following technical scheme:
A kind of fraise jig, comprise T shape seat for being connected with the milling machine substrate and and the bolted chuck body of T shape seat, the side of described chuck body is provided with the screwed hole of perforation, in described screwed hole, is provided with hold-down bolt, and the head of described hold-down bolt is provided with compact heap.T shape seat is put into the draw-in groove on the milling machine substrate, tight a bolt and make chuck body and T shape seat be fixed on the milling machine substrate, fix several fixtures around workpiece, compact heap is withstood to the side of workpiece, then tighten hold-down bolt, compact heap on fixture has just been located Work-sheet pressing like this, can not be subject to the effect of fixture on to be processed of workpiece, therefore only need clamping once just can complete the Milling Process on the whole plane of workpiece, thereby guarantee crudy and machining accuracy, the out-of-flatness of the mismachining tolerance of avoiding secondary clamping to bring and tool marks junction.
As preferably, the cross section of described compact heap is right angled triangle, comprise the trailing flank that ,He bottom surface, bottom surface is vertical and the inclined-plane that connects bottom surface and trailing flank, the trailing flank of described compact heap is connected with the head of hold-down bolt, the bottom surface of described compact heap is parallel with the milling machine substrate, and the bottom surface of compact heap is provided with the support raised line.The tip portion of compact heap withstands side surface of workpiece, support raised line and milling machine substrate contacts, thereby make the tip of compact heap fix on the middle part of side surface of workpiece, more stable after holding out against, compact heap is inclined-plane near the face of workpiece, can effectively prevent the interference between cutter and compact heap.
As preferably, the head of described compact heap is fixed with wear plate.Wear plate hardness is high, wear-resistant, can increase the service life of fixture.
As preferably, on described chuck body, with the both sides of the junction of T shape seat, extend to form limited block.Just snap in T shape seat between two limited blocks, so can not mutually rotate between T shape seat and chuck body, guarantee can not cause because of the rotation between chuck body and T shape seat workpiece loosening after the fixture top tight workpiece.
As preferably, described hold-down bolt is provided with pre-load nut.After hold-down bolt is tightened, compact heap workpiece pressing side, then tighten the pre-load nut on hold-down bolt, prevents that workpiece is in process, and hold-down bolt becomes flexible and causes workpiece loosening.
As preferably, between the plane at described hold-down bolt and milling machine substrate place, structure in an angle.When turning hold-down bolt, existence due to angle, make the power acted on hold-down bolt resolve into two component, a component workpiece pressing side parallel with the milling machine substrate, another component vertically acts on the bottom surface and the milling machine substrate that make compact heap on the milling machine substrate and tightly fits, thereby guarantee the stability of fixture, workpiece process can not shake.
As preferably, the side of described chuck body also is provided with standby screwed hole, in described preparation screwed hole, is provided with standby hold-down bolt.After long-term the use, have between hold-down bolt and screwed hole after wearing and tearing cause becoming flexible and can use standby screwed hole and standby hold-down bolt, thus the service life of improving whole fixture.
Therefore, the utlity model has and can guarantee the just whole workpiece planarization of energy Milling Process of clamped one time, thus the beneficial effect of assurance machining accuracy and crudy.
The accompanying drawing explanation
Fig. 1 is a kind of structural representation of the present utility model.
Fig. 2 is front view of the present utility model.
In figure: T shape seat 1 chuck body 2 hold-down bolt 3 compact heaps 4 support raised line 5 wear plate 6 limited block 7 pre-load nut 8 hold-down bolts 9.
The specific embodiment
Below in conjunction with the drawings and specific embodiments, the utility model is further described:
A kind of fraise jig as depicted in figs. 1 and 2, comprise T shape seat 1 for being connected with the milling machine substrate and and the bolted chuck body 2 of T shape seat, the side of chuck body 2 is provided with the screwed hole of perforation, be provided with hold-down bolt 3 in screwed hole, hold-down bolt 3 is provided with pre-load nut 8, the head of hold-down bolt 3 passes screwed hole and is provided with compact heap 4, the cross section of compact heap 4 is right angled triangle, comprise bottom surface, the trailing flank vertical with bottom surface and be connected bottom surface and the inclined-plane of trailing flank, the trailing flank of compact heap 4 is connected with the head of hold-down bolt 3, the bottom surface of compact heap 4 is parallel with the milling machine substrate, the bottom surface of compact heap is provided with supports raised line 5, the tip portion of compact heap withstands side surface of workpiece, support raised line and milling machine substrate contacts, thereby the tip that makes compact heap fixes on the middle part of side surface of workpiece, more stable after holding out against, compact heap is inclined-plane near the face of workpiece, can effectively prevent the interference between cutter and compact heap, the binding face that supports raised line and milling machine substrate is arc surface, the head of compact heap 4 is fixed with wear plate 6, wear plate is made by cutter material, such as wolfram steel is made, there is higher hardness, wear-resisting effective, can strengthen the service life of fixture, the contact jaw of wear plate and workpiece is a very little plane, can top tight workpiece, can not cause obvious impression again, between the plane at hold-down bolt 3 and milling machine substrate place, structure in an angle, angle is 20 degree, when turning hold-down bolt, existence due to angle, make the power acted on hold-down bolt resolve into two component, a component workpiece pressing side parallel with the milling machine substrate, another component vertically acts on the bottom surface and the milling machine substrate that make compact heap on the milling machine substrate and tightly fits, thereby guarantee the stability of fixture, workpiece process can not shake, extend to form limited block 7 with the both sides of the junction of T shape seat 1 on chuck body 2, limited block can effectively prevent from mutually rotating between chuck body and T shape seat, the side of chuck body 2 also is provided with standby screwed hole, be provided with standby hold-down bolt 9 in described preparation screwed hole, after long-term the use, have between hold-down bolt and screwed hole after wearing and tearing cause becoming flexible and can use standby screwed hole and standby hold-down bolt, thus the service life of improving whole fixture.
By reference to the accompanying drawings, using method of the present utility model is as follows, smooth being placed on the milling machine substrate workpiece, in the both sides of workpiece, the T-slot of corresponding milling machine substrate is placed a plurality of this kind of fixtures, T shape seat snaps in T-slot, then turn hold-down bolt, make the compact heap workpiece pressing side on each fixture, now can carry out Milling Process, add man-hour, the direction of feed of milling cutter is vertical with the limit of the workpiece at fixture place, workpiece is more stable during Milling Process like this, due on the upper surface of workpiece without any the interference of thing, after clamping, a milling just can complete the processing on whole plane, machining accuracy is high, flatness is good.Therefore, the utlity model has and can guarantee the just whole workpiece planarization of energy Milling Process of clamped one time, thus the beneficial effect of assurance machining accuracy and crudy.

Claims (7)

1. 一种铣床夹具,包括用于和铣床基板连接的T形座(1)以及和T形座螺栓连接的夹具本体(2),其特征是,所述的夹具本体(2)的侧面设有贯通的螺纹孔,所述的螺纹孔内设有压紧螺栓(3),所述的压紧螺栓(3)的头部设有压紧块(4)。 1. A milling machine fixture, including a T-shaped seat (1) used to connect with the milling machine base plate and a fixture body (2) connected with T-shaped seat bolts, characterized in that, the side of the fixture body (2) is designed There is a through threaded hole, the said threaded hole is provided with a compression bolt (3), and the head of the said compression bolt (3) is provided with a compression block (4). 2.根据权利要求1所述的一种铣床夹具,其特征是,所述的压紧块(4)的横截面为直角三角形,包括底面、和底面垂直的后侧面以及连接底面和后侧面的斜面,所述的压紧块(4)的后侧面与压紧螺栓(3)的头部连接,所述的压紧块(4)的底面与铣床基板平行,压紧块的底面上设有支撑凸条(5)。 2. A milling machine fixture according to claim 1, characterized in that the cross-section of the pressing block (4) is a right triangle, including a bottom surface, a rear side perpendicular to the bottom surface, and a connection between the bottom surface and the rear side Inclined surface, the rear side of the pressing block (4) is connected to the head of the pressing bolt (3), the bottom surface of the pressing block (4) is parallel to the base plate of the milling machine, and the bottom surface of the pressing block is provided with Support ribs (5). 3.根据权利要求2所述的一种铣床夹具,其特征是,所述的压紧块(4)的头部固定有耐磨片(6)。 3. A milling machine clamp according to claim 2, characterized in that, the head of the pressing block (4) is fixed with a wear-resistant plate (6). 4.根据权利要求1所述的一种铣床夹具,其特征是,所述的夹具本体(2)上与T形座(1)的连接处的两侧延伸形成限位块(7)。 4. A milling machine clamp according to claim 1, characterized in that, the two sides of the connection between the clamp body (2) and the T-shaped seat (1) extend to form limit blocks (7). 5.根据权利要求1所述的一种铣床夹具组,其特征是,所述的压紧螺栓(3)上设有预紧螺母(8)。 5. A milling machine fixture set according to claim 1, characterized in that a pre-tightening nut (8) is provided on the pressing bolt (3). 6.根据权利要求1或5所述的一种铣床夹具,其特征是,所述的压紧螺栓(3)与铣床基板所在的平面之间构成一个夹角。 6. A milling machine fixture according to claim 1 or 5, characterized in that, an angle is formed between the pressing bolt (3) and the plane where the milling machine base plate is located. 7.根据权利要求1或4所述的一种铣床夹具,其特征是,所述的夹具本体(2)的侧面还设有备用螺纹孔,所述的预备螺纹孔内设有备用压紧螺栓(9)。 7. A milling machine fixture according to claim 1 or 4, characterized in that, the side of the fixture body (2) is also provided with a spare threaded hole, and a spare compression bolt is arranged in the said preparatory threaded hole (9).
CN 201220568521 2012-10-31 2012-10-31 A milling machine fixture Expired - Fee Related CN202934376U (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN 201220568521 CN202934376U (en) 2012-10-31 2012-10-31 A milling machine fixture

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN 201220568521 CN202934376U (en) 2012-10-31 2012-10-31 A milling machine fixture

Publications (1)

Publication Number Publication Date
CN202934376U true CN202934376U (en) 2013-05-15

Family

ID=48318635

Family Applications (1)

Application Number Title Priority Date Filing Date
CN 201220568521 Expired - Fee Related CN202934376U (en) 2012-10-31 2012-10-31 A milling machine fixture

Country Status (1)

Country Link
CN (1) CN202934376U (en)

Cited By (6)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN107598631A (en) * 2017-11-10 2018-01-19 禹州市伟朔机械制造厂 A kind of movable wedge
CN109676522A (en) * 2018-11-22 2019-04-26 成都飞机工业(集团)有限责任公司 Semi-automatic stress compensates clamping device
CN109909773A (en) * 2019-03-25 2019-06-21 杜安 The convenient general side fixture of slope surface slidingtype
CN115255990A (en) * 2022-08-16 2022-11-01 山西平阳重工机械有限责任公司 Milling fixture for thin plate part surface
CN121245258A (en) * 2025-11-03 2026-01-02 四川航天长征装备制造有限公司 Positioning method of flexible tool for laser cutting of several frames
CN121267408A (en) * 2025-11-03 2026-01-06 四川航天长征装备制造有限公司 Flexible frock of several type frame laser cutting

Cited By (6)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN107598631A (en) * 2017-11-10 2018-01-19 禹州市伟朔机械制造厂 A kind of movable wedge
CN109676522A (en) * 2018-11-22 2019-04-26 成都飞机工业(集团)有限责任公司 Semi-automatic stress compensates clamping device
CN109909773A (en) * 2019-03-25 2019-06-21 杜安 The convenient general side fixture of slope surface slidingtype
CN115255990A (en) * 2022-08-16 2022-11-01 山西平阳重工机械有限责任公司 Milling fixture for thin plate part surface
CN121245258A (en) * 2025-11-03 2026-01-02 四川航天长征装备制造有限公司 Positioning method of flexible tool for laser cutting of several frames
CN121267408A (en) * 2025-11-03 2026-01-06 四川航天长征装备制造有限公司 Flexible frock of several type frame laser cutting

Similar Documents

Publication Publication Date Title
CN203019089U (en) Moving lathe end beam boring mill clamp
CN201313255Y (en) Fixture used for processing bevel at small end of connecting rod
CN202356947U (en) Special fixture for lathe processing of thin-walled disc workpieces
CN102350649B (en) A kind of work piece holder of Digit Control Machine Tool
CN202655958U (en) Processing and clamping fixture for inclined top of die
CN203228039U (en) Milling clamp for multiple cylindrical workpieces
CN203579273U (en) Vice special for rotary machining center
CN102441801A (en) Fixture board for milling small flange for exhaust pipe
CN202162590U (en) Workpiece clamping device for milling end surfaces of workpieces
CN208034157U (en) Clamping jig for round piece
CN210335214U (en) Clamping tool for machining inclined-tooth steam seal end surface step and radiation surface
CN204868248U (en) Reverse gear and shift cantilever at anchor clamps of machine with central end face milling
CN220516127U (en) Horizontal machining center clamp for pump body
CN207710348U (en) Ozzle mutually passes through Machining of Curved Surface positioning tool
CN205271448U (en) Anchor clamps of ultra -thin shape work piece of high -efficient processing
CN202639934U (en) Combined side top plate
CN202804724U (en) Differential mechanism drilling hole tool
CN203779161U (en) Flat square part milling tooling for roller shaft
CN202622560U (en) Upper die universal grinding clamp
CN216967050U (en) Clamp for processing on peeling machine knife rest box tensioning bevel connection lathe
CN216966405U (en) A processing tool for a peeling machine tool holder on a slotting machine
CN223933115U (en) Machining fixture of shot-blasting machine backplate
CN204818856U (en) A anchor clamps that is used for machining center to mill cantilever terminal surface of shifting gears that reverses gear
CN206998327U (en) A kind of guide plate packaged type flower disc clamp
CN204868091U (en) High -efficient reliable reversing gear cantilever positioning fixture of shifting

Legal Events

Date Code Title Description
C14 Grant of patent or utility model
GR01 Patent grant
CP01 Change in the name or title of a patent holder

Address after: 315800 No. 1528 Hengshan Road, Xintao Street, Beilun District, Ningbo City, Zhejiang Province

Co-patentee after: Ji'nan Geely Auto Parts Co., Ltd.

Patentee after: Zhejiang Geely Power Assembly Co., Ltd.

Co-patentee after: Hunan Luoyou Engine Parts Co., Ltd.

Co-patentee after: Zhejiang Geely Holding Group Co., Ltd.

Address before: 315800 No. 1528 Hengshan Road, Xintao Street, Beilun District, Ningbo City, Zhejiang Province

Co-patentee before: Ji'nan Geely Auto Parts Co., Ltd.

Patentee before: Zhejiang Geely Luoyou Engine Co., Ltd.

Co-patentee before: Hunan Luoyou Engine Parts Co., Ltd.

Co-patentee before: Zhejiang Geely Holding Group Co., Ltd.

CP01 Change in the name or title of a patent holder
CF01 Termination of patent right due to non-payment of annual fee

Granted publication date: 20130515

Termination date: 20201031

CF01 Termination of patent right due to non-payment of annual fee