CN202491344U - Mold opening delaying mechanism - Google Patents
Mold opening delaying mechanism Download PDFInfo
- Publication number
- CN202491344U CN202491344U CN2012200499321U CN201220049932U CN202491344U CN 202491344 U CN202491344 U CN 202491344U CN 2012200499321 U CN2012200499321 U CN 2012200499321U CN 201220049932 U CN201220049932 U CN 201220049932U CN 202491344 U CN202491344 U CN 202491344U
- Authority
- CN
- China
- Prior art keywords
- block
- push pedal
- opening mechanism
- mold
- push plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Landscapes
- Moulds For Moulding Plastics Or The Like (AREA)
Abstract
一种延迟开模机构,应用于模具中,该延迟开模机构包括:拨块,其一端固定于母模板一侧,该拨块设有容纳槽,设有容纳槽的该端设有凸块;挡块,其一端设于所述推板中,另一端伸出该推板,且该挡块与该推板间设有弹性元件;锁紧块,其一端固定于公模板一侧,另一端设于所述容纳槽中,且设于容纳槽的该端设有勾块,该勾块卡住所述挡块;拉杆,其从所述下固定板及公模板及推板中穿过,且该拉杆一端固定于所述母模仁中,模具开模时该拉杆另一端卡设在推板中从而固定推板。本实用新型的延迟开模机构,在生产筒类产品时,通过拨块拨动所述挡块从而控制开模顺序,且该延迟开模机构能够省掉公模仁、角垫及顶出机构,结构简单。
A delayed mold opening mechanism, which is used in molds, and the delayed mold opening mechanism includes: a shifting block, one end of which is fixed on one side of a mother template, the shifting block is provided with a receiving groove, and the end of the receiving groove is provided with a protrusion ; block, one end of which is located in the push plate, the other end protrudes from the push plate, and an elastic element is provided between the block and the push plate; locking block, one end is fixed on one side of the male template, and the other One end is arranged in the accommodating groove, and the end of the accommodating groove is provided with a hook block, and the hook block clamps the block; a pull rod passes through the lower fixing plate, the male template and the push plate , and one end of the pull rod is fixed in the core of the female mold, and the other end of the pull rod is clamped in the push plate when the mold is opened to fix the push plate. The delayed mold opening mechanism of the utility model controls the mold opening sequence by moving the block through the dial when producing tube products, and the delayed mold opening mechanism can save the male mold core, corner pad and ejection mechanism ,Simple structure.
Description
【技术领域】 【Technical field】
本实用新型涉及一种模具机构,具体涉及一种解决四次开模顺序的延迟开模机构。The utility model relates to a mold mechanism, in particular to a delayed mold opening mechanism which solves the four-time mold opening sequence.
【背景技术】 【Background technique】
在塑胶产品的生产中,一些筒类和一些壳类产品四周侧壁很高,中间形体很少,粘模力最大的地方就在四周侧壁处,如果很小的圆筒用常规的套筒顶出即可;如果筒类产品比较大或者是方形的或不规则的形体时,用常规的顶出不便于排顶针,生产此类产品的模具更适合采用推板顶出,然而此类模具具有四次开模动作,四次开模顺序需要先后安排好。In the production of plastic products, some cylinders and some shell products have very high side walls and few intermediate shapes. The place with the greatest sticking force is on the side walls. If a small cylinder uses a conventional sleeve Ejection is enough; if the cylindrical product is relatively large or square or irregular in shape, it is not convenient to use conventional ejection to arrange ejector pins. The mold for producing such products is more suitable for ejection with push plate. However, this type of mold There are four mold opening actions, and the order of the four mold openings needs to be arranged successively.
鉴于以上问题,实有必要提供一种延迟开模机构,该延迟开模机构能够很好的解决四次开模的顺序。In view of the above problems, it is necessary to provide a delayed mold opening mechanism, which can well solve the sequence of four mold openings.
【发明内容】 【Content of invention】
因此,本实用新型的目的是提供一种延迟开模机构,该延迟开模机构能够很好的解决四次开模的顺序。Therefore, the purpose of the utility model is to provide a delayed mold opening mechanism, which can well solve the sequence of four mold openings.
为了达到上述目的,本实用新型的延迟开模机构,应用于模具中,该模具自上而下依次包括:上固定板、剥料板、母模板、母模仁、公模入子、推板、公模板及下固定板,该延迟开模机构包括:In order to achieve the above purpose, the delayed mold opening mechanism of the present utility model is applied in the mold, and the mold includes from top to bottom: an upper fixing plate, a stripping plate, a female template, a female mold core, a male mold insert, and a push plate , public formwork and lower fixed plate, the delayed mold opening mechanism includes:
拨块,其一端固定于所述母模板一侧,该拨块设有容纳槽,设有容纳槽的该端设有凸块;A shifting block, one end of which is fixed on one side of the mother template, the shifting block is provided with a receiving groove, and the end of the receiving groove is provided with a protrusion;
挡块,其一端设于所述推板中,另一端伸出该推板,且该挡块与该推板间设有弹性元件,模具开模时所述拨块通过凸块拨动该挡块使其完全退回到推板中,从而使模具开模;A block, one end of which is arranged in the push plate, and the other end protrudes from the push plate, and an elastic element is arranged between the block and the push plate, and the block is moved by the bump when the mold is opened. The block makes it fully retreat into the push plate, so that the mold is opened;
锁紧块,其一端固定于所述公模板一侧,另一端设于所述容纳槽中,且设于容纳槽的该端设有勾块,该勾块卡住所述挡块,模具开模时该勾块与该挡块脱离;Locking block, one end of which is fixed on one side of the male template, the other end is arranged in the accommodating groove, and the end of the accommodating groove is provided with a hook block, and the hook block clamps the block, and the mold is opened. The hook block is disengaged from the stopper during molding;
拉杆,其从所述下固定板及公模板及推板中穿过,且该拉杆一端固定于所述母模仁中,模具开模时该拉杆另一端卡设在推板中从而固定推板。Pull rod, which passes through the lower fixing plate, the male template and the push plate, and one end of the pull rod is fixed in the core of the female mold, and the other end of the pull rod is clamped in the push plate to fix the push plate when the mold is opened .
特别地,所述推板中设有相应的容纳空间以供所述挡块设于其中。In particular, a corresponding accommodating space is provided in the push plate for the stopper to be disposed therein.
特别地,所述弹性元件为弹簧。In particular, the elastic element is a spring.
特别地,该挡块上设有卡槽,该卡槽与该推板间设有限位螺丝以限位该挡块。In particular, a card slot is provided on the stop block, and a limit screw is provided between the card slot and the push plate to limit the stop block.
特别地,所述凸块上设有第一斜面。In particular, the protrusion is provided with a first slope.
特别地,所述挡块伸出推板的该端设有第二斜面,该第二斜面与所述第一斜面倾斜角度相同。In particular, the end of the stopper protruding from the push plate is provided with a second slope, and the angle of inclination of the second slope is the same as that of the first slope.
特别地,所述下固定板及公模板及推板中设有相应的容纳空间以供所述拉杆从中穿过。In particular, corresponding accommodating spaces are provided in the lower fixing plate, the male plate and the push plate for the pull rods to pass through.
相较于现有技术,本实用新型的延迟开模机构,在生产筒类产品时,通过拨块拨动所述挡块从而控制开模顺序,且该延迟开模机构能够省掉公模仁、角垫及顶出机构,结构简单。Compared with the prior art, the delayed mold opening mechanism of the present utility model controls the mold opening sequence by moving the stopper through the dial when producing tube products, and the delayed mold opening mechanism can save the male mold core. , Corner pads and ejection mechanism, simple structure.
【附图说明】 【Description of drawings】
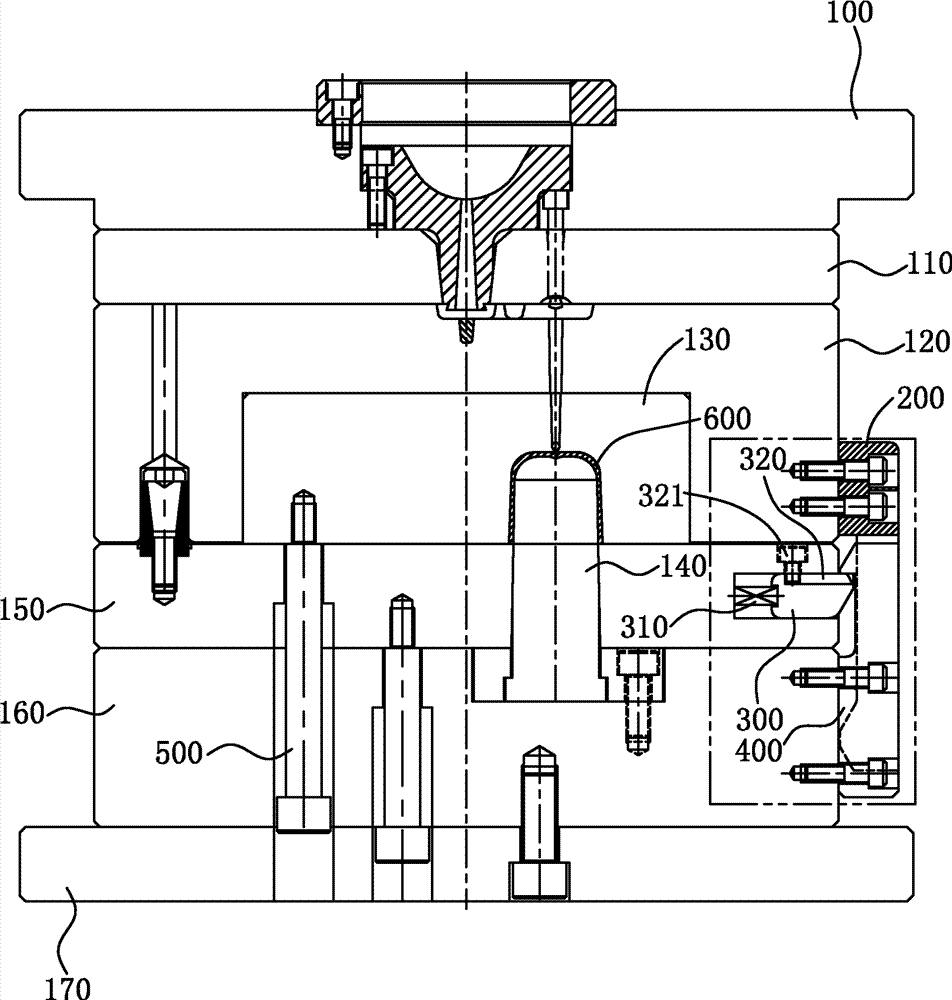
图1绘示本实用新型延迟开模机构于模具合模状态的示意图。FIG. 1 shows a schematic diagram of the delayed mold opening mechanism of the present invention in a mold closing state.
图2绘示图1的局部放大示意图。FIG. 2 is a partially enlarged schematic diagram of FIG. 1 .
图3绘示图2局部放大图的侧面示意图。FIG. 3 is a schematic side view of a partially enlarged view of FIG. 2 .
图4绘示本实用新型延迟开模机构于模具第三次开模状态的示意图。FIG. 4 is a schematic diagram of the delayed mold opening mechanism of the present invention in the mold opening state for the third time.
图5绘示本实用新型延迟开模机构于模具第四次开模状态的示意图。FIG. 5 shows a schematic diagram of the delayed mold opening mechanism of the present invention in the fourth mold opening state of the mold.
【具体实施方式】 【Detailed ways】
请同时参阅图1、图2及图3,于本实施例中,本实用新型的延迟开模机构,其应用于模具中,该模具自上而下依次包括:上固定板100、剥料板110、母模板120、母模仁130、公模入子140、推板150、公模板160及下固定板170,该延迟开模机构包括:Please refer to Fig. 1, Fig. 2 and Fig. 3 at the same time. In this embodiment, the delayed mold opening mechanism of the present utility model is applied in a mould. 110.
拨块200,其一端固定于所述母模板120一侧,该拨块200设有容纳槽220,设有容纳槽220的该端设有凸块210,该凸块210上设有第一斜面211;The shifting
挡块300,其一端设于所述推板150中,该推板150中设有相应的容纳空间以供该挡块300设于其中,该挡块300另一端伸出该推板150,伸出推板150的该端设有第二斜面330,该第二斜面330与所述第一斜面211倾斜角度相同,且该挡块300与该推板150间于水平方向上设有弹性元件310,于本实施例中该弹性元件310为弹簧,于模具开模时所述拨块200通过凸块210拨动该挡块300使其完全退回到推板150中,从而使模具开模,另外该挡块300上设有卡槽320,该卡槽320与该推板150间于竖直方向上设有限位螺丝321以限位该挡块300,防止该挡块300从推板150中脱离;
锁紧块400,其一端固定于所述公模板160一侧,另一端设于所述容纳槽220中,且设于容纳槽220的该端设有勾块410,该勾块410卡住所述挡块300,于模具开模时该勾块410与该挡块300脱离;
拉杆500,其从所述下固定板170及公模板160及推板150中穿过,该下固定板170及公模板160及推板150中设有相应的容纳空间以供该拉杆500从中穿过,且该拉杆500一端固定于所述母模仁130中,模具开模时该拉杆500另一端卡设在推板150中从而固定推板150,使其停止运动。The
当模具开模时,第一次开模及第二次开模与普通三板模一样,即第一次开模时剥料板110与母模板120分开将产品600与流道分开,第二次开模时剥料板110与上固定板100分开将流道从模具中剥落。When the mold is opened, the first mold opening and the second mold opening are the same as the ordinary three-platen mold, that is, the
请参阅图4所示,模具第三次开模时,公模板160继续运动,由于锁紧块400的勾块410卡住了挡块300从而与挡块300锁在一起,使公模板160和推板150不能分开,使公模板160与推板150一起运动远离母模板120,产品600的包紧力使产品600与母模仁130分开留在公模入子140上,完成产品600的分模。Please refer to shown in Fig. 4, when the mold is opened for the third time, the
请参阅图5所示,模具第四次开模时,公模板160与推板150继续运动,当拉杆500另一端卡在推板150中时,推板150完成运动行程而停止运动;由于第一斜面211与第二斜面330的相互配合作用,拨块200凸块210拨动挡块300,弹性元件310被压缩,挡块300在拨块200的凸块210的拨动作用下,完全退回到推板150内;而锁紧块400的勾块410不再卡着挡块300,使锁紧块400和挡块300脱离,公模板160与推板150分开;公模板160继续运动直至公模入子140与产品600完全脱模后,完成模具的第四次开模;产品600与公模入子140脱离后将产品600取出。Please refer to shown in Figure 5, when the mold is opened for the fourth time, the
相较于现有技术,本实用新型的延迟开模机构,在生产筒类产品时,通过拨块拨动所述挡块从而控制开模顺序,且该延迟开模机构能够省掉公模仁、角垫及顶出机构,结构简单。Compared with the prior art, the delayed mold opening mechanism of the present utility model controls the mold opening sequence by moving the stopper through the dial when producing tube products, and the delayed mold opening mechanism can save the male mold core. , Corner pads and ejection mechanism, simple structure.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012200499321U CN202491344U (en) | 2012-02-16 | 2012-02-16 | Mold opening delaying mechanism |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012200499321U CN202491344U (en) | 2012-02-16 | 2012-02-16 | Mold opening delaying mechanism |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202491344U true CN202491344U (en) | 2012-10-17 |
Family
ID=46997583
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012200499321U Expired - Lifetime CN202491344U (en) | 2012-02-16 | 2012-02-16 | Mold opening delaying mechanism |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202491344U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103252857A (en) * | 2012-02-16 | 2013-08-21 | 汉达精密电子(昆山)有限公司 | Mold opening delaying mechanism |
| CN105946181A (en) * | 2016-07-06 | 2016-09-21 | 健大电业制品(昆山)有限公司 | Injection mold facilitating pulling-out of material belt |
-
2012
- 2012-02-16 CN CN2012200499321U patent/CN202491344U/en not_active Expired - Lifetime
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103252857A (en) * | 2012-02-16 | 2013-08-21 | 汉达精密电子(昆山)有限公司 | Mold opening delaying mechanism |
| CN103252857B (en) * | 2012-02-16 | 2016-12-21 | 汉达精密电子(昆山)有限公司 | Postpone die opening mechanism |
| CN105946181A (en) * | 2016-07-06 | 2016-09-21 | 健大电业制品(昆山)有限公司 | Injection mold facilitating pulling-out of material belt |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205310722U (en) | Novel second grade ejection mechanism | |
| CN103817878B (en) | Forced demoulding mechanism | |
| CN103921411B (en) | Secondary ejecting mechanism | |
| CN105291382A (en) | Core pulling injection die used in inner-and-outer multiple directions | |
| CN103252857B (en) | Postpone die opening mechanism | |
| CN201361970Y (en) | Injection mold ejecting mechanism | |
| CN202293121U (en) | Dual-oblique-pin mechanism | |
| CN203254622U (en) | Double-inverted-buckle product de-molding device in injection mold | |
| CN203293487U (en) | Flexible pipe plug injection mold | |
| CN202062602U (en) | Product back-off detaching mechanism | |
| CN203198181U (en) | Two-step ejection mechanism | |
| CN105269768B (en) | The three oblique pulled core structures of template die master mold | |
| CN202293240U (en) | Ejection mechanism of injection mold | |
| CN203650779U (en) | Double-ejection structure | |
| CN107791463B (en) | Female die inclined core-pulling withdrawing structure | |
| CN204451026U (en) | The pressure return structure of mould | |
| CN203092861U (en) | Sliding block withdrawal mechanism | |
| CN201848973U (en) | injection mold | |
| CN201120682Y (en) | Plastic mold | |
| CN104723504A (en) | Mould glue injection structure | |
| CN102285034A (en) | Secondary ejection forced release mechanism | |
| CN204149468U (en) | Flexible glue cast gate delayed ejection structure | |
| CN204295967U (en) | The oblique pulled core structure of master mold | |
| CN201712092U (en) | Secondary ejection and forced demolding mechanism | |
| CN202952513U (en) | Three-plate die opening and closing die sequence controller |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant |