CN202475182U - Shaping device of motor coil - Google Patents
Shaping device of motor coil Download PDFInfo
- Publication number
- CN202475182U CN202475182U CN201120515534XU CN201120515534U CN202475182U CN 202475182 U CN202475182 U CN 202475182U CN 201120515534X U CN201120515534X U CN 201120515534XU CN 201120515534 U CN201120515534 U CN 201120515534U CN 202475182 U CN202475182 U CN 202475182U
- Authority
- CN
- China
- Prior art keywords
- link block
- base
- shaping
- supporting base
- curved surface
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000007493 shaping process Methods 0.000 title claims abstract description 33
- 230000000295 complement effect Effects 0.000 claims 7
- 239000012528 membrane Substances 0.000 claims 6
- 239000012530 fluid Substances 0.000 claims 4
- 238000003825 pressing Methods 0.000 abstract description 38
- 230000007246 mechanism Effects 0.000 abstract description 9
- 230000006835 compression Effects 0.000 description 8
- 238000007906 compression Methods 0.000 description 8
- 238000000034 method Methods 0.000 description 6
- 238000004519 manufacturing process Methods 0.000 description 5
- 238000010586 diagram Methods 0.000 description 3
- 238000001125 extrusion Methods 0.000 description 3
- 238000009413 insulation Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000010720 hydraulic oil Substances 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
Images



Landscapes
- Manufacture Of Motors, Generators (AREA)
Abstract
一种电机线圈的整形装置,包括上模组件、下模组件和液压驱动装置;上模组件的顶板的左右两侧分别装有若干个侧压模导轨,每一个上侧压模件的铰支座分别与相应的侧压模导轨滑移配合,每一个上侧压模件还分别与装在侧压模导轨上的相应的复位机构相连,两个直边上压模块分别装在顶板的前后两侧;下模组件的底座的左右两侧分别装有若干下模块导轨,第一支承座和第二支承座分别与相应的下模块导轨滑移配合,所述若干下侧导向架的铰支座分别固定在相应的第一支承座和第二支承座上,两个直边下压模块分别装在底座的前后两侧;所述下模组件的底座的左右两侧分别固定有液压驱动装置。本实用新型不仅结构简单,而且能保证电机线圈一致性、工作效率高。
A shaping device for motor coils, comprising an upper mold assembly, a lower mold assembly and a hydraulic drive device; the left and right sides of the top plate of the upper mold assembly are respectively equipped with several side pressing mold guide rails, and each upper pressing mold part The hinge supports are respectively slidingly matched with the corresponding side die guide rails, and each upper side die part is also respectively connected with the corresponding reset mechanism installed on the side die guide rails, and the two straight side upper press modules are respectively installed on the The front and rear sides of the top plate; the left and right sides of the base of the lower mold assembly are respectively equipped with a number of lower module guide rails, and the first support base and the second support base are respectively slidably matched with the corresponding lower module guide rails. The hinge supports of the frame are respectively fixed on the corresponding first support base and the second support base, and the two straight-side pressing modules are installed on the front and rear sides of the base respectively; the left and right sides of the base of the lower mold assembly are respectively Fixed hydraulic drive. The utility model not only has a simple structure, but also can ensure the consistency of the motor coil and high working efficiency.
Description
技术领域 technical field
本实用新型涉及一种用于制造大功率牵引电机过程中使用的工装,具体地说涉及一种用于大功率牵引电机线圈的整形装置,属于电机制造领域。 The utility model relates to a tool used in the process of manufacturing a high-power traction motor, in particular to a shaping device for the coil of a high-power traction motor, which belongs to the field of motor manufacturing. the
背景技术 Background technique
大功率牵引电机线圈制造过程中,需要对线圈进行涨形。现有的国产涨形机用于大功率牵引电机线圈涨形时,存在以下缺点:第一、由于液压系统不稳定,顶弧装置只有一个支点,因而使用时强度不够;第二,涨形臂运行速度不一致,导致涨形后的线圈之间的外形尺寸、形状差异较大,不能保证一致性;第三,由于机械夹钳的螺栓易松动,设备精度较差,因而不能满足后续嵌线工序对线圈之间最小间隙的要求。因此,在涨形过程中,为了保证线圈圆角处的尺寸和形状,还需要进行人工敲击整形,而这样容易使线圈绝缘层破损,不仅增加操作人员的劳动强度,而且降低了牵引电机的可靠性和使用寿命。又由于涨形机设备精度和后续绝缘包扎工序的影响,导致线圈的直线边部分变形,需要工人手持线圈,只能用装有专用工装的气动台钳对直线边部分进行整形,每次只能整形一小段,需要操作人员多次移动线圈,多次操作才能完成一个线圈的整形,不仅工作效率低,而且劳动强度高。在嵌线过程中,需要用专用工具调整线圈形状以及尺寸;在相邻线圈端部对应部位之间间隙不均匀时,或者线圈鼻端外侧高度不一致时,都需要人工敲击整形,这样不仅工作效率低、劳动强度高,而且容易使线圈上包扎的绝缘层破损,降低了电机的可靠性和使用寿命。目前进口的涨形机可以解决以上问题,但结构复杂、成本太高。 In the manufacturing process of high-power traction motor coils, the coils need to be expanded. When the existing domestically-made stretching machines are used for stretching the coils of high-power traction motors, there are the following disadvantages: first, due to the unstable hydraulic system, the top arc device has only one fulcrum, so the strength is not enough when used; second, the stretching arm The running speed is inconsistent, resulting in a large difference in the size and shape of the expanded coils, and the consistency cannot be guaranteed; third, because the bolts of the mechanical clamp are easy to loosen, the accuracy of the equipment is poor, so it cannot meet the subsequent wire embedding process Requirements for minimum clearance between coils. Therefore, in the expansion process, in order to ensure the size and shape of the coil fillet, it is necessary to perform manual knocking and shaping, and this will easily damage the coil insulation layer, which not only increases the labor intensity of the operator, but also reduces the traction motor. reliability and service life. In addition, due to the influence of the equipment precision of the expander and the subsequent insulation wrapping process, the straight edge of the coil is partially deformed, requiring workers to hold the coil, and the straight edge can only be shaped with a pneumatic vise equipped with special tooling. For a short section of shaping, the operator needs to move the coil multiple times, and the shaping of a coil can only be completed through multiple operations, which is not only low in work efficiency, but also high in labor intensity. In the process of inserting the wire, it is necessary to use special tools to adjust the shape and size of the coil; when the gap between the corresponding parts of the adjacent coil ends is uneven, or when the height of the outer side of the coil nose is inconsistent, it is necessary to manually knock the shape, which not only works The efficiency is low, the labor intensity is high, and the insulating layer wrapped on the coil is easily damaged, which reduces the reliability and service life of the motor. The currently imported stretching machine can solve the above problems, but the structure is complicated and the cost is too high. the
发明内容 Contents of the invention
本实用新型的目的是克服现有技术的不足,提供一种不仅结构简单,能保证牵引电机的可靠性、线圈的一致性、工作效率高,而且成本低的电机线圈的整形装置。 The purpose of the utility model is to overcome the deficiencies of the prior art and provide a motor coil shaping device with a simple structure, which can ensure the reliability of the traction motor, the consistency of the coil, high work efficiency, and low cost. the
实现上述目的的技术方案是:一种电机线圈的整形装置,其创新点在于:包括上模组件、下模组件和液压驱动装置; The technical solution to achieve the above purpose is: a shaping device for motor coils, the innovation of which is that it includes an upper mold assembly, a lower mold assembly and a hydraulic drive device;
所述上模组件包括顶板、若干个带有铰支座和压头的上侧压模件、两个直边上压模块和若干个复位机构,所述顶板的左右两侧分别装有若干个侧压模导轨,每一个上侧压模件的铰支座分别与相应的侧压模导轨滑移配合,每一个上侧压模件的铰支座还分别与装在侧压模导轨上的相应的复位机构相连,两个直边上压模块分别装在顶板的前后两侧; The upper mold assembly includes a top plate, several upper side pressing modules with hinged supports and pressure heads, two straight-side upper pressing modules and several reset mechanisms, and the left and right sides of the top plate are equipped with several Each side die guide rail, the hinge support of each upper side die part is slidingly matched with the corresponding side die guide rail respectively, and the hinge support of each upper side die part is also installed on the side die guide rail respectively. The corresponding reset mechanism is connected, and the two straight-side pressing modules are respectively installed on the front and rear sides of the top plate;
所述下模组件包括底座、第一支承座、第二支承座、若干个带有铰支座的下侧导向架、两个直边下压模块、第一连接模块和第二连接模块,所述底座的左右两侧分别装有若干个下模块导轨,第一支承座和第二支承座分别与相应的下模块导轨滑移配合,所述若干个下侧导向架的铰支座分别固定在相应的第一支承座和第二支承座上,所述底座上的左右侧分别装有第一连接模块和第二连接模块,且第一连接模块和第二连接模块分别位于第一支承座和第二支承座的内侧,两个直边下压模块分别固定在第一连接模块和第二连接模块的前后端; The lower mold assembly includes a base, a first support seat, a second support seat, several lower side guide frames with hinge supports, two straight-side pressing modules, a first connection module and a second connection module, The left and right sides of the base are respectively equipped with several lower module guide rails, the first support seat and the second support seat respectively slide and cooperate with the corresponding lower module guide rails, and the hinge supports of the several lower side guide frames are respectively fixed On the corresponding first support seat and second support seat, the left and right sides of the base are respectively equipped with a first connection module and a second connection module, and the first connection module and the second connection module are respectively located on the first support seat and the inner side of the second support base, two straight-side pressing modules are respectively fixed at the front and rear ends of the first connection module and the second connection module;
所述下模组件的底座的左右两侧分别固定有液压驱动装置,第一支承座和第二支承座分别与相应的液压驱动装置的活塞杆装连; The left and right sides of the base of the lower mold assembly are respectively fixed with hydraulic drive devices, and the first support base and the second support base are respectively connected with the piston rods of the corresponding hydraulic drive devices;
所述下侧导向架均具有导向孔,上模组件运动时,上侧压模件的压头能分别插入相应的下侧导向架的导向孔内,两个直边上压模块能与两个直边下压模块对齐。 The lower side guide frames all have guide holes. When the upper mold assembly moves, the indenters of the upper side dies can be respectively inserted into the guide holes of the corresponding lower side guide frames. Align with two straight-edged push-down modules.
在上述技术方案中,所述上模组件的装在侧压模导轨上的复位机构包括复位弹簧、支杆、安装座和弹簧套,所述安装座固定在侧压模导轨上,所述支杆穿过安装座,支杆的一端伸入弹簧套内且与弹簧套固定连接,所述复位弹簧套在支杆上,复位弹簧一端与安装座相抵,另一端与弹簧套内的挡肩相抵,弹簧套与上侧压模件的铰支座内侧相抵,铰支座外侧的侧压模导轨上具有侧压模限位块。 In the above technical solution, the reset mechanism of the upper mold assembly mounted on the side die guide rail includes a return spring, a pole, a mounting seat and a spring sleeve, the mounting seat is fixed on the side die guide rail, and the The pole passes through the mounting seat, and one end of the pole extends into the spring sleeve and is fixedly connected with the spring sleeve. Offset, the spring cover and the inner side of the hinge support of the upper side compression mold are offset, and the side compression mold guide rails outside the hinge support have side compression mold limit blocks. the
在上述技术方案中,所述上模组件的顶板的左右两端外侧分别装有导向套,下模组件的第一支承座和第二支承座上分别装有导向柱,所述导向柱能插入对应的导向套且与导向套滑动配合。 In the above technical solution, guide sleeves are installed on the outer sides of the left and right ends of the top plate of the upper mold assembly, and guide columns are respectively installed on the first support base and the second support base of the lower mold assembly. The corresponding guide sleeve can be inserted and slidably matched with the guide sleeve. the
在上述技术方案中,所述底座上的第一连接模块通过定距螺栓与第二连接模块固定连接。 In the above technical solution, the first connection module on the base is fixedly connected to the second connection module by distance bolts. the
在上述技术方案中,所述的第一连接模块上具有与线圈两侧底部曲面相匹配的第一定形曲面,第二连接模块上具有与线圈两侧底部曲面相匹配的第二定形曲面;第一连接模块还具有与线圈两侧内侧的曲面相匹配的第一侧面定形曲面,第二连接模块还具有与线圈两侧内侧的曲面相匹配的第二侧面定形曲面。 In the above technical solution, the first connecting module has a first shaped curved surface matching the bottom curved surfaces on both sides of the coil, and the second connecting module has a second shaped curved surface matching the bottom curved surfaces on both sides of the coil; The first connection module also has a first side shaped curved surface that matches the inner curved surfaces on both sides of the coil, and the second connection module also has a second side shaped curved surface that matches the inner curved surfaces on both sides of the coil. the
在上述技术方案中,所述上模组件的每一个上侧压模件的压头底部均设有第一折角槽口,两个直边上压模块上分别设有第二折角槽口;所述下模组件的两个直边下压模块上分别设有第三折角槽口。 In the above technical solution, the bottom of the press head of each of the upper die components of the upper die assembly is provided with a first angled notch, and the two straight-side upper pressing modules are respectively provided with a second angled notch; The two straight-side pressing modules of the lower mold assembly are respectively provided with third corner notches. the
在上述技术方案中,所述上侧压模件的压头底部的曲面与对应部位的第一连接模块的第一定形曲面和第二连接模块的第二定形曲面相匹配;压头底部的第一折角槽口的上曲面与线圈两侧相应部位的顶部曲面相匹配,压头底部的第一折角槽口的外侧曲面与线圈两侧相应部位的外侧曲面相匹配。 In the above technical solution, the curved surface at the bottom of the indenter of the upper die part matches the first shaped curved surface of the first connection module and the second shaped curved surface of the second connected module at the corresponding position; the bottom of the indenter The upper curved surface of the first knuckle notch matches the top curved surface of corresponding parts on both sides of the coil, and the outer curved surface of the first knuckle notch at the bottom of the indenter matches the outer curved surface of corresponding parts on both sides of the coil. the
在上述技术方案中,所述每一个上侧压模件的铰支座的顶部均设有滑座,所述滑座分别与相应的侧压模导轨滑移配合;所述第一支承座和第二支承座的底部分别设有相应的第一滑座和第二滑座,第一滑座和第二滑座分别与相应的下模块导轨滑移配合。 In the above technical solution, the top of the hinge support of each of the upper side dies is provided with a sliding seat, and the sliding seats are slidingly matched with the corresponding side die guide rails; the first support seat and The bottom of the second supporting seat is respectively provided with a corresponding first sliding seat and a second sliding seat, and the first sliding seat and the second sliding seat are slidingly matched with corresponding lower module guide rails respectively. the
在上述技术方案中,所述上模组件的顶板上设有顶板豁口,下模组件的底座上也相应设有底座豁口。 In the above technical solution, a top plate opening is provided on the top plate of the upper mold assembly, and a base opening is correspondingly provided on the base of the lower mold assembly. the
在上述技术方案中,所述液压驱动装置为液压油缸。 In the above technical solution, the hydraulic drive device is a hydraulic oil cylinder. the
本实用新型的有益效果在于:本实用新型包括上模组件、下模组件和液压驱动装置;所述上模组件包括顶板、若干带铰支座的上侧压模件、两个直边上压模块和若干复位机构;所述下模组件包括底座、第一支承座、第二支承座、若干带铰支座的下侧导向架、两个直边下压模块、第一连接模块和第二连接模块;所述下模组件的底座的左右两侧分别固定有液压驱动装置,第一支承座和第二支承座分别与相应的液压驱动装置的活塞杆装连;本实用新型使用时,先将上模组件安装在液压机的滑块上,下模组件安装在液压机的工作台上,接着将电机线圈套在下模组件的两个直边下压模块、第一连接模块和第二连接模块上,然后启动液压驱动装置,带动第一支承座和第二支承座以及带铰支座的下侧导向架向中间移动到设定位置后即可停止,操作液压机,使得安装在液压机的滑块上的上模组件向下运动,上侧压模件的压头部分别插入相应的下侧导向架的导向孔内且继续向下运动,使得上侧压模件对电机线圈外周的斜边部分进行挤压,同时,两个直边上压模块也对电机线圈的直边部分进行挤压,待挤压完毕后取下电机线圈即可;本实用新型不仅结构简单、而且能够保证牵引电机线圈的形状和尺寸的一致性、质量稳定可靠,在电机线圈涨形和嵌线时不需要人工敲击整形,避免了人工敲击整形导致的质量隐患,同时降低了劳动强度;本实用新型可以同时对牵引电机线圈的两个直边部分和四个斜边部分进行整形,不再需要对直边部分单独进行整形,大大提高了工作效率,降低了劳动强度。此外,本实用新型仅需要与普通液压机配套使用即可,与进口涨形机相比,不仅结构简单,而且设备成本大大降低。 The beneficial effects of the utility model are: the utility model includes an upper mold assembly, a lower mold assembly and a hydraulic drive device; Side pressing modules and several reset mechanisms; the lower mold assembly includes a base, a first support seat, a second support seat, several lower side guide frames with hinged supports, two straight side pressing modules, a first connection module and the second connection module; the left and right sides of the base of the lower mold assembly are respectively fixed with hydraulic drive devices, and the first support base and the second support base are respectively connected to the piston rods of the corresponding hydraulic drive devices; the utility model When the new model is used, the upper mold assembly is first installed on the slider of the hydraulic press, the lower mold assembly is installed on the workbench of the hydraulic press, and then the motor coil is placed on the two straight-side pressing modules of the lower mold assembly. Connect the module and the second connection module, and then start the hydraulic drive device, drive the first support seat, the second support seat and the lower side guide frame with the hinged support to move to the middle to the set position and then stop, operate the hydraulic press, Make the upper mold assembly installed on the slide block of the hydraulic press move downward, the indenter heads of the upper side die parts are respectively inserted into the guide holes of the corresponding lower side guide frame and continue to move downward, so that the upper side die parts Squeeze the hypotenuse part of the outer circumference of the motor coil, and at the same time, two straight-side pressing modules also squeeze the straight part of the motor coil, and the motor coil can be removed after the extrusion is completed; the utility model not only has a structure It is simple, and can ensure the consistency of the shape and size of the traction motor coil, and the quality is stable and reliable. It does not need manual knocking and shaping when the motor coil is expanded and embedded, avoiding the quality hazards caused by manual knocking and shaping, and at the same time reducing Labor intensity: the utility model can simultaneously reshape two straight parts and four hypotenuse parts of the traction motor coil, and no longer needs to reshape the straight parts separately, which greatly improves work efficiency and reduces labor intensity. In addition, the utility model only needs to be used in conjunction with ordinary hydraulic presses. Compared with imported stretching machines, the utility model not only has a simple structure, but also greatly reduces equipment costs. the
附图说明 Description of drawings
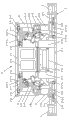
图1为本实用新型的结构示意图; Fig. 1 is the structural representation of the utility model;
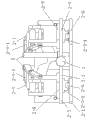
图2为图1中上模组件的仰视图; Fig. 2 is the bottom view of upper mold assembly in Fig. 1;
图3为图2的C向旋转图,也即图2的左视旋转图; Fig. 3 is a C-direction rotation diagram of Fig. 2, that is, a left-side rotation diagram of Fig. 2;
图4为图2中沿A-A方向的剖视旋转图; Fig. 4 is the sectional rotation diagram along A-A direction in Fig. 2;
图5为图1中下模组件的结构示意图; Fig. 5 is the structural representation of lower mold assembly in Fig. 1;
图6为图1中下模组件的俯视图; Fig. 6 is the top view of lower mold assembly in Fig. 1;
图7为图5的右视图; Fig. 7 is the right view of Fig. 5;
图8为图6沿B-B方向的剖视图; Fig. 8 is a sectional view along the B-B direction of Fig. 6;
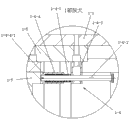
图9为图4中I部放大图; Fig. 9 is an enlarged view of part I in Fig. 4;
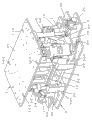
图10为本实用新型的立体示意图。 Fig. 10 is a perspective view of the utility model.
具体实施方式 Detailed ways
以下结合附图,对本实用新型作进一步详细描述。 Below in conjunction with accompanying drawing, the utility model is described in further detail. the
如图1~10所示,一种电机线圈的整形装置,包括上模组件1、下模组件2和液压驱动装置3;所述上模组件1包括顶板1-1、若干个带有铰支座1-7和压头1-8的上侧压模件1-2、两个直边上压模块1-3和若干个复位机构1-4,所述顶板1-1的左右两侧分别装有若干个侧压模导轨1-5,每一个上侧压模件1-2的铰支座1-7分别与相应的侧压模导轨1-5滑移配合,每一个上侧压模件1-2的铰支座1-7还分别与装在侧压模导轨1-5上的相应的复位机构1-4相连,两个直边上压模块1-3分别装在顶板1-1的前后两侧;所述下模组件2包括底座2-1、第一支承座2-2、第二支承座2-3、若干个带有铰支座2-9的下侧导向架2-4、两个直边下压模块2-5、第一连接模块2-7和第二连接模块2-8,所述底座2-1的左右两侧分别装有若干个下模块导轨2-6,第一支承座2-2和第二支承座2-3分别与相应的下模块导轨2-6滑移配合,所述若干个下侧导向架2-4的铰支座2-9分别固定在相应的第一支承座2-2和第二支承座2-3上,所述底座2-1上的左右侧分别装有第一连接模块2-7和第二连接模块2-8,且第一连接模块2-7和第二连接模块2-8分别位于第一支承座2-2和第二支承座2-3的内侧,两个直边下压模块2-5分别固定在第一连接模块2-7和第二连接模块2-8的前后端;所述下模组件2的底座2-1的左右两侧分别固定有液压驱动装置3,第一支承座2-2和第二支承座2-3分别与相应的液压驱动装置3的活塞杆3-1装连;所述下侧导向架2-4均具有导向孔2-4-1,上模组件1运动时,上侧压模件1-2的压头1-8能分别插入相应的下侧导向架2-4的导向孔2-4-1内,两个直边上压模块1-3能与两个直边下压模块2-5对齐。 As shown in Figures 1 to 10, a shaping device for motor coils includes an upper mold assembly 1, a lower mold assembly 2 and a hydraulic drive device 3; the upper mold assembly 1 includes a top plate 1-1, several belts There are hinged support 1-7 and the upper side pressing module 1-2 of pressing head 1-8, two straight-edge upper pressing modules 1-3 and several reset mechanisms 1-4, the left and right sides of the top plate 1-1 Several side die guide rails 1-5 are respectively installed on both sides, and the hinge support 1-7 of each upper side die part 1-2 slides and cooperates with the corresponding side die guide rails 1-5 respectively, and each upper die guide rail 1-5 The hinge support 1-7 of side pressing module 1-2 also links to each other with the corresponding resetting mechanism 1-4 that is contained on the side pressing mold guide rail 1-5 respectively, and two straight edge upper pressing modules 1-3 are contained in respectively The front and rear sides of the top plate 1-1; the lower mold assembly 2 includes a base 2-1, a first support seat 2-2, a second support seat 2-3, and several lower hinge supports 2-9. Side guide frame 2-4, two straight side pressing modules 2-5, first connection module 2-7 and second connection module 2-8, the left and right sides of the base 2-1 are respectively equipped with several lower The module guide rails 2-6, the first support base 2-2 and the second support base 2-3 are slidingly matched with the corresponding lower module guide rails 2-6 respectively, and the hinge supports of the several lower side guide frames 2-4 2-9 are respectively fixed on the corresponding first support base 2-2 and second support base 2-3, and the left and right sides of the base 2-1 are respectively equipped with a first connection module 2-7 and a second connection module 2-8, and the first connection module 2-7 and the second connection module 2-8 are respectively located on the inside of the first support seat 2-2 and the second support seat 2-3, and the two straight-edge pressing modules 2-5 They are respectively fixed at the front and rear ends of the first connection module 2-7 and the second connection module 2-8; the left and right sides of the base 2-1 of the lower mold assembly 2 are respectively fixed with a hydraulic drive device 3, and the first support seat 2-2 and the second supporting seat 2-3 are respectively connected with the piston rod 3-1 of the corresponding hydraulic drive device 3; the lower guide frame 2-4 has a guide hole 2-4-1, and the upper module When the part 1 moves, the pressure head 1-8 of the upper side die part 1-2 can be inserted into the guide hole 2-4-1 of the corresponding lower side guide frame 2-4 respectively, and the two straight-sided upper pressing modules 1- 3 can be aligned with two straight edge pressing modules 2-5. the
本实用新型的上侧压模件1-2和下侧导向架2-4分别为四个,并且使用独立的液压驱动装置3作为动力源,能够实现带铰支座2-9的下侧导向架2-4自动向两侧或者向中间移动,方便整形前摆放电机线圈,以及整形后取出电机线圈。
The utility model has four upper side pressing modules 1-2 and lower side guide frames 2-4 respectively, and uses an independent
如图1、5、6、7、8所示,所示液压油缸驱动装置3为液压油缸。
As shown in Figures 1, 5, 6, 7 and 8, the hydraulic
如图1、2、4、9所示,为了保证所述上侧压模件1-2的压头1-8能够准确插入相应的下侧导向架2-4的导向孔2-4-1内,并且能够复位,所述上模组件1的装在侧压模导轨1-5上的复位机构1-4包括复位弹簧1-4-1、支杆1-4-2、安装座1-4-3和弹簧套1-4-4,所述安装座1-4-3固定在侧压模导轨1-5上,所述支杆1-4-2穿过安装座1-4-3,支杆1-4-2的一端伸入弹簧套1-4-4内且与弹簧套1-4-4固定连接,所述复位弹簧1-4-1套在支杆1-4-2上,复位弹簧1-4-1一端与安装座1-4-3相抵,另一端与弹簧套1-4-4内的挡肩1-4-4-1相抵,弹簧套1-4-4与上侧压模件1-2的铰支座1-7内侧相抵,铰支座1-7外侧的侧压模导轨1-5上具有侧压模限位块1-6。整形结束后,当上侧压模件1-2向上移动时,在上侧压模件1-2的最低点脱离下侧导向架2-4的导向孔2-4-1后,支杆1-4-2在复位弹簧1-4-1的作用下通过铰支座1-7推动上侧压模件1-2沿侧压模导轨1-5向外侧移动,以及在复位机构1-4和侧压模限位块1-6的共同作用下,上侧压模件1-2保持在固定位置,这样可以保证电机线圈每次整形时,上侧压模件1-2都可以从正确的位置进入下侧导向架2-4的导向孔2-4-1。
As shown in Figures 1, 2, 4, and 9, in order to ensure that the indenter 1-8 of the upper die part 1-2 can be accurately inserted into the guide hole 2-4-1 of the corresponding lower guide frame 2-4 Inside, and can be reset, the reset mechanism 1-4 of the
如图1、2、3、4、5、6、7、8、10所示,为了实现将上模组件1和下模组件2精确定位,所述上模组件1的顶板1-1的左右两端外侧分别装有导向套4,下模组件2的第一支承座2-2和第二支承座2-3上分别装有导向柱5,所述导向柱5能插入对应的导向套4且与导向套4滑动配合。
As shown in Figures 1, 2, 3, 4, 5, 6, 7, 8, and 10, in order to achieve accurate positioning of the
如图1、5、6、8、10所示,为了适用多种尺寸规格的电机线圈,所述底座2-1上的第一连接模块2-7通过定距螺栓6与第二连接模块2-8固定连接。当需要对不同直边部分尺寸的线圈进行整形时,只需要更换直边上压模块1-3和直边下压模块2-5,并通过调节定距螺栓6来调节第一连接模块2-7和第二连接模块2-8之间的距离,即可满足不同直边部分尺寸电机线圈的制造要求;当需要对不同尺寸规格的线圈进行整形时,只需要更换直边上压模块1-3、直边下压模块2-5、第一连接模块2-7和第二连接模块2-8、上侧压模件1-2的压头1-8,并通过调节定距螺栓6来调节第一连接模块2-7和第二连接模块2-8之间的距离,即可满足不同电机线圈的制造要求。
As shown in Figures 1, 5, 6, 8, and 10, in order to be suitable for motor coils of various sizes and specifications, the first connection module 2-7 on the base 2-1 is connected to the
如图1、5、6、8、10所示,为了使得线圈的曲面部分与第一连接模块2-7和第二连接模块2-8相匹配,所述的第一连接模块2-7上具有与线圈两侧底部曲面相匹配的第一定形曲面2-7-1,第二连接模块2-8上具有与线圈两侧底部曲面相匹配的第二定形曲面2-8-1;第一连接模块2-7还具有与线圈两侧内侧的曲面相匹配的第一侧面定形曲面2-7-2,第二连接模块2-8还具有与线圈两侧内侧的曲面相匹配的第二侧面定形曲面2-8-2。 As shown in Figures 1, 5, 6, 8, and 10, in order to make the curved part of the coil match the first connection module 2-7 and the second connection module 2-8, the first connection module 2-7 It has a first shaped curved surface 2-7-1 that matches the bottom curved surfaces on both sides of the coil, and the second connecting module 2-8 has a second shaped curved surface 2-8-1 that matches the bottom curved surfaces on both sides of the coil; A connection module 2-7 also has a first side shaping curved surface 2-7-2 that matches the curved surfaces on both sides of the coil inside, and a second connection module 2-8 also has a second curved surface that matches the inside curved surfaces on both sides of the coil. The side shaping surface is 2-8-2. the
如图2、3、4、6、8所示,为了使得电机整形效果佳,保证线圈的形状和尺寸的一致性,所述上模组件1的每一个上侧压模件1-2的压头1-8的底部均设有第一折角槽口1-8-1,两个直边上压模块1-3上分别设有第二折角槽口1-3-1;所述下模组件2的两个直边下压模块2-5上分别设有第三折角槽口2-5-1;所述上侧压模件1-2的压头1-8底部的曲面与对应部位的第一连接模块2-7的第一定形曲面2-7-1和第二连接模块2-8的第二定形曲面2-8-1相匹配;压头1-8底部的第一折角槽口1-8-1的上曲面1-8-2与线圈两侧相应部位的顶部曲面相匹配,压头1-8底部的第一折角槽口1-8-1的外侧曲面1-8-3与线圈两侧相应部位的外侧曲面相匹配。整形时,电机线圈直边部分和斜边部分分别能够嵌在相应的上侧压模件1-2的第一折角槽口1-8-1、直边上压模块1-3的第二折角槽口1-3-1、直边下压模块2- 5的第三折角槽口2-5-1、第一连接模块2-7的第一定形曲面2-7-1、第一侧面定形曲面2-7-2和第二连接模块2-8的第二定形曲面二2-8-1、第二侧面定形曲面2-8-2之间,实现同时对电机线圈直边部分和斜边部分两个方向的挤压整形。 As shown in Figures 2, 3, 4, 6, and 8, in order to make the motor shaping effect better and ensure the consistency of the shape and size of the coil, each upper side pressing mold part 1-2 of the upper mold assembly 1 The bottom of the indenter 1-8 is provided with a first angled notch 1-8-1, and the two straight-side upper pressing modules 1-3 are respectively provided with a second angled notch 1-3-1; The two straight side pressing modules 2-5 of the component 2 are respectively provided with a third angled notch 2-5-1; the curved surface at the bottom of the pressing head 1-8 of the upper side pressing module 1-2 corresponds The first shaped curved surface 2-7-1 of the first connection module 2-7 of the position matches the second shaped curved surface 2-8-1 of the second connected module 2-8; the first curved surface at the bottom of the indenter 1-8 The upper curved surface 1-8-2 of the knuckle notch 1-8-1 matches the top curved surface of the corresponding parts on both sides of the coil, and the outer curved surface 1-8-1 of the first knuckle notch 1-8-1 at the bottom of the indenter 1-8 8-3 matches the outer curved surfaces of the corresponding parts on both sides of the coil. During shaping, the straight side part and the hypotenuse part of the motor coil can respectively be embedded in the first knuckle notch 1-8-1 of the corresponding upper side pressing module 1-2, and the second knuckle of the straight side upper pressing module 1-3 Notch 1-3-1, the third knuckle notch 2-5-1 of the straight side pressing module 2-5, the first shaping surface 2-7-1 of the first connection module 2-7, the first side Between the second shaped curved surface 2-7-2 and the second shaped curved surface 2-8-1 of the second connection module 2-8, and the second side shaped curved surface 2-8-2, the straight side part and the inclined part of the motor coil can be realized simultaneously. Extrusion shaping in both directions of the edge part. the
如图1、3、4、5、7、8所示,为了便于上侧压模件1-2的铰支座1-7与侧压模导轨1-5以及第一支承座2-2和第二支承座2-3与相应的下模块导轨2-6滑移配合,所述每一个上侧压模件1-2的铰支座1-7的顶部均设有滑座1-7-1,所述滑座1-7-1分别与相应的侧压模导轨1-5滑移配合;所述第一支承座2-2和第二支承座2-3的底部分别设有相应的第一滑座2-2-1和第二滑座2-3-1,第一滑座2-2-1和第二滑座2-3-1分别与相应的下模块导轨2-6滑移配合。 As shown in Figures 1, 3, 4, 5, 7, and 8, in order to facilitate the hinge support 1-7 of the upper side die part 1-2 and the side die guide rail 1-5 and the first support seat 2-2 and The second support seat 2-3 is slidingly matched with the corresponding lower module guide rail 2-6, and the top of the hinge support 1-7 of each upper side die part 1-2 is provided with a sliding seat 1-7- 1. The sliding seats 1-7-1 are slidably matched with the corresponding side die guide rails 1-5; the bottoms of the first supporting seat 2-2 and the second supporting seat 2-3 are respectively equipped with The first sliding seat 2-2-1 and the second sliding seat 2-3-1, the first sliding seat 2-2-1 and the second sliding seat 2-3-1 slide with the corresponding lower module guide rail 2-6 respectively shift fit. the
如图1、2、3、4、8、10所示,为了便于与液压机的工作台以及滑块装连,所述上模组件1的顶板1-1上设有顶板豁口1-1-1,下模组件2的底座2-1上也相应设有底座豁口2-1-1。
As shown in Figures 1, 2, 3, 4, 8, and 10, in order to facilitate the installation and connection with the workbench and slider of the hydraulic press, the top plate 1-1 of the
本实用新型适用于各种类型的电机线圈的整形,特别适用于大功率牵引电机线圈的整形。 The utility model is suitable for shaping various types of motor coils, and is especially suitable for shaping the coils of high-power traction motors. the
本实用新型使用时,先将上模组件1通过顶板1-1安装在液压机的滑块上,下模组件2通过底座2-1安装在液压机的工作台上,操作液压机使其滑块提升至设定高度,在滑块提升到设定高度后,所述上模组件1的上侧压模件1-2的最低点比下模组件2的下侧导向架2-4的最高点高50mm以上;然后启动位于底座2-1左右两侧的液压驱动装置3,下模组件2的第一支承座2-2和第二支承座2-3以及相应带铰支座2-9的下侧导向架2-4在液压驱动装置3的驱动下,沿着相应的下模块导轨2-6向两侧移动,移动到位后自动停止;将电机线圈套在下模组件2的两个直边下压模块2-5的第三折角槽口2-5-1上,再次操作液压驱动装置3,下模组件2的第一支承座2-2和第二支承座2-3以及相应带铰支座2-9的下侧导向架2-4在液压驱动装置3的驱动下,沿着相应的下模块导轨2-6向中间移动,移动到位后自动停止;操作液压机使其滑块向下移动,且下移至指定高度时,上侧压模件1-2插入下侧导向架2-4的导向孔2-4-1内,上侧压模件1-2在导向孔2-4-1的约束下继续向下移动,上侧压模件1-2的第一折角槽口1-8-1对电机线圈斜边部分的上表面以及侧面方向进行挤压;同时,直边上压模块1-3在向下移动的过程中,直边上压模块1-3的第二折角槽口1-3-1对电机线圈直边部分的上表面以及侧面进行挤压;在上侧压模件1-2的压头1-8底部的曲面与对应部位的第一连接模块的第一定形曲面2-7-1和第二连接模块的第二定形曲面2-8-1吻合时停止挤压,操作液压机使其滑块提升至设定高度,操作液压驱动装置3,第一支承座2-2和第二支承座2-3以及相应带铰支座2-9的下侧导向架2-4在液压驱动装置3驱动下,沿着相应的下模块导轨2-6向两侧移动,移动到位后自动停止,这时人工取下电机线圈,整形完毕。
When the utility model is used, the
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201120515534XU CN202475182U (en) | 2011-12-13 | 2011-12-13 | Shaping device of motor coil |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201120515534XU CN202475182U (en) | 2011-12-13 | 2011-12-13 | Shaping device of motor coil |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202475182U true CN202475182U (en) | 2012-10-03 |
Family
ID=46923305
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201120515534XU Expired - Lifetime CN202475182U (en) | 2011-12-13 | 2011-12-13 | Shaping device of motor coil |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202475182U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102664498A (en) * | 2011-12-13 | 2012-09-12 | 江苏常牵庞巴迪牵引系统有限公司 | Motor coil reshaping apparatus |
| CN104253515A (en) * | 2014-08-14 | 2014-12-31 | 周嘉成 | Movement mechanism of expanding machine and expanding machine with movement mechanism |
| CN107612246A (en) * | 2017-10-11 | 2018-01-19 | 六安江淮电机有限公司 | The not damaged setting process of HV Electric Machine Coil |
| CN112311161A (en) * | 2020-10-28 | 2021-02-02 | 中车株洲电机有限公司 | Linear edge shaping device for forming winding coil |
-
2011
- 2011-12-13 CN CN201120515534XU patent/CN202475182U/en not_active Expired - Lifetime
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102664498A (en) * | 2011-12-13 | 2012-09-12 | 江苏常牵庞巴迪牵引系统有限公司 | Motor coil reshaping apparatus |
| CN102664498B (en) * | 2011-12-13 | 2014-04-02 | 江苏常牵庞巴迪牵引系统有限公司 | Motor coil reshaping apparatus |
| CN104253515A (en) * | 2014-08-14 | 2014-12-31 | 周嘉成 | Movement mechanism of expanding machine and expanding machine with movement mechanism |
| CN107612246A (en) * | 2017-10-11 | 2018-01-19 | 六安江淮电机有限公司 | The not damaged setting process of HV Electric Machine Coil |
| CN107612246B (en) * | 2017-10-11 | 2019-03-19 | 六安江淮电机有限公司 | The not damaged setting process of HV Electric Machine Coil |
| CN112311161A (en) * | 2020-10-28 | 2021-02-02 | 中车株洲电机有限公司 | Linear edge shaping device for forming winding coil |
| CN112311161B (en) * | 2020-10-28 | 2022-07-05 | 中车株洲电机有限公司 | A linear edge shaping device for forming winding coils |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102729066B (en) | Clamp for processing positioning hole on engine cylinder cover | |
| CN105479028A (en) | Three-station stator press-fitting welding machine | |
| CN204893363U (en) | Automobile engine is last to sell mechanism with camshaft from dynamic pressure | |
| CN111250949A (en) | Press mounting device for check valve of cylinder cover of automobile engine | |
| CN102896449B (en) | Framework assembling tire | |
| CN111482857B (en) | Surface treatment system after forming of metallurgical casting connecting piece | |
| CN110977385B (en) | Automatic bolt assembling equipment for rear end plate of automobile engine | |
| CN203679592U (en) | Adjustable welding tool | |
| CN204321545U (en) | Knuckle bushing pressing machine | |
| CN102664498B (en) | Motor coil reshaping apparatus | |
| CN200974168Y (en) | Bidirectional pneumatic press-loading machine | |
| CN206010357U (en) | A kind of suspension spring compacting machine | |
| CN107716620A (en) | General die casting seamless tool | |
| CN203599509U (en) | Device for removing riser head of vehicle wheel blank side die | |
| CN216954987U (en) | Universal fixture for high-voltage test of clamp | |
| CN202668126U (en) | Fixture for machining positioning hole of motor cylinder cover | |
| CN107186408B (en) | Piling car carriage assembly tool | |
| CN206567381U (en) | A kind of auto parts and components mechanical pressure machine worktable of mobile work | |
| CN203578145U (en) | Flattening mechanism for axle housing gumming surface flattening mechanism | |
| CN209223094U (en) | Unloading mechanism for hydraulic press | |
| CN211990356U (en) | Bending machine | |
| CN209598540U (en) | Wirerope rope guide clamping tooling | |
| CN202174235U (en) | Gravity casting machine for hydraulic aluminum casting | |
| CN207577164U (en) | General die casting seamless jig | |
| CN219360045U (en) | Large-stroke double-layer demoulding structure |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| AV01 | Patent right actively abandoned |
Granted publication date: 20121003 Effective date of abandoning: 20140402 |
|
| RGAV | Abandon patent right to avoid regrant |