CN116213527A - A method for operating a continuous three-step stamping die device for a three-wheeled motorcycle edge cover - Google Patents
A method for operating a continuous three-step stamping die device for a three-wheeled motorcycle edge cover Download PDFInfo
- Publication number
- CN116213527A CN116213527A CN202310086058.1A CN202310086058A CN116213527A CN 116213527 A CN116213527 A CN 116213527A CN 202310086058 A CN202310086058 A CN 202310086058A CN 116213527 A CN116213527 A CN 116213527A
- Authority
- CN
- China
- Prior art keywords
- die
- supporting
- bending
- mold
- stamping
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D7/00—Bending rods, profiles, or tubes
- B21D7/06—Bending rods, profiles, or tubes in press brakes or between rams and anvils or abutments; Pliers with forming dies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D28/00—Shaping by press-cutting; Perforating
- B21D28/02—Punching blanks or articles with or without obtaining scrap; Notching
- B21D28/14—Dies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D35/00—Combined processes according to or processes combined with methods covered by groups B21D1/00 - B21D31/00
- B21D35/002—Processes combined with methods covered by groups B21D1/00 - B21D31/00
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D43/00—Feeding, positioning or storing devices combined with, or arranged in, or specially adapted for use in connection with, apparatus for working or processing sheet metal, metal tubes or metal profiles; Associations therewith of cutting devices
- B21D43/003—Positioning devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D43/00—Feeding, positioning or storing devices combined with, or arranged in, or specially adapted for use in connection with, apparatus for working or processing sheet metal, metal tubes or metal profiles; Associations therewith of cutting devices
- B21D43/02—Advancing work in relation to the stroke of the die or tool
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
- Forging (AREA)
Abstract
一种三轮摩托车包边套连续三步冲压模具装置的操作方法,下模座上方设置上模座,下模座的上侧面中部从左到右依次设置冲形底模、第一支撑模和第二支撑模,上模座的下侧面中部从左到右依次设置冲形顶模、第一折弯模和第二折弯模,冲形顶模与冲形底模相互扣合,第一支撑模和第一折弯模相互扣合,第二折弯模和第二支撑模相互扣合,第一折弯模的一侧设置脱料机构;本发明结构简单、使用方便,能够通过上模座和下模座的扣合,同步完成金属板材的冲压成形、第一次折弯和第二次折弯三步冲压工序,在制成包边套后,能够通过退料气缸和退料顶板使制成的包边套脱离冲压模具,无需工人过多干预,有效的保障了各道工序的连续形,能够大幅度提高生产效率。
An operation method for a continuous three-step stamping die device for a three-wheeled motorcycle side cover. An upper die base is arranged above the lower die base, and a punching bottom die and a first support die are sequentially arranged on the middle part of the upper side of the lower die base from left to right. and the second supporting mold, the middle part of the lower side of the upper mold base is arranged in turn from left to right in the punching top mold, the first bending mold and the second bending mold, the punching top mold and the punching bottom mold are interlocked, the first A supporting mold and the first bending mold are interlocked, the second bending mold and the second supporting mold are interlocked, and a stripping mechanism is arranged on one side of the first bending mold; the invention is simple in structure and easy to use, and can pass through The fastening of the upper mold base and the lower mold base simultaneously completes the three-step stamping process of stamping forming, first bending and second bending of the metal sheet. The material top plate makes the hemming sleeve made out of the stamping die, without too much intervention by workers, which effectively guarantees the continuous shape of each process and can greatly improve production efficiency.
Description
技术领域technical field
本发明涉及三轮摩托车包边套生产技术领域,尤其涉及一种三轮摩托车包边套连续三步冲压模具装置的操作方法。The invention relates to the technical field of production of three-wheeled motorcycle hemming sleeves, in particular to an operation method for a continuous three-step stamping die device for three-wheeled motorcycle hemming sleeves.
背景技术Background technique
三轮摩托车包边套是用于三轮摩托车箱体上,对三轮摩托车箱体上的方管进行包边的方形金属套,其是通过对金属板进行冲压折弯制成,目前,在对三轮摩托车包边套冲压制作时,需要先从金属板材上截取所要形状和规格金属板,再将金属板的边缘部两侧和中部两侧分别通过不同的冲压模具进行九十度折弯,在操作过程中,每次冲压都需要在不同的冲压模具上进行,频繁更换冲压模具不仅操作繁琐、生产效率低下,而且需要更多的人工投入,增加了生产成本。因此,怎样解决目前在对三轮摩托车包边套冲压制作时,每次冲压都需要在不同的冲压模具上进行导致的操作繁琐、生产效率低下的问题,成为长期以来难以解决的技术难题。The three-wheeled motorcycle wrapping sleeve is a square metal sleeve used on the three-wheeled motorcycle box to wrap the square tube on the three-wheeled motorcycle box. It is made by stamping and bending the metal plate. At present, when stamping the edge cover of a three-wheeled motorcycle, it is necessary to cut out the metal plate of the desired shape and specification from the metal plate, and then pass the two sides of the edge and the middle of the metal plate through different stamping dies. Ten-degree bending, in the operation process, each stamping needs to be carried out on a different stamping die, frequent replacement of stamping dies is not only cumbersome to operate, low in production efficiency, but also requires more labor input, which increases production costs. Therefore, how to solve the problems of cumbersome operation and low production efficiency caused by the need for each stamping to be carried out on different stamping dies when stamping the side cover of the three-wheeled motorcycle at present has become a technical problem that has been difficult to solve for a long time.
鉴于上述原因,现研发一种三轮摩托车包边套连续三步冲压模具装置的操作方法。In view of the above reasons, the operation method of a continuous three-step stamping die device of a three-wheeled motorcycle edge cover is now developed.
发明内容Contents of the invention
本发明是为了克服现有技术的不足,提供一种三轮摩托车包边套连续三步冲压模具装置的操作方法,能够通过上模座和下模座的扣合,同步完成金属板材的冲压成形、第一次折弯和第二次折弯三步冲压工序, 在制成包边套后,能够通过退料气缸和退料顶板使制成的包边套脱离冲压模具,无需工人过多干预,有效的保障了各道工序的连续形,能够大幅度提高生产效率、节省工人体力和用工数量、降低生产成本,有效的解决了目前在对三轮摩托车包边套冲压制作时,每次冲压都需要在不同的冲压模具上进行导致的操作繁琐、生产效率低下的问题。The purpose of the present invention is to overcome the deficiencies of the prior art, and to provide a continuous three-step stamping die device operation method for the side cover of a three-wheeled motorcycle, which can synchronously complete the stamping of the metal plate through the fastening of the upper mold base and the lower mold base Three-step stamping process of forming, first bending and second bending. After the hemming sleeve is made, the finished hemming sleeve can be separated from the stamping die through the ejection cylinder and the ejection top plate, without requiring too many workers Intervention effectively guarantees the continuous shape of each process, can greatly improve production efficiency, save workers' physical strength and labor, and reduce production costs. Each stamping needs to be carried out on different stamping dies, resulting in cumbersome operations and low production efficiency.
本发明为了实现上述目的,采用如下技术方案:一种三轮摩托车包边套连续三步冲压模具装置的操作方法,所述的一种三轮摩托车包边套连续三步冲压模具装置,是由:下模座、上模座、冲形底模、第一支撑模、第二支撑模、冲形顶模、第一折弯模、第二折弯模、顶模容腔、成形部、外凸部、滑轨、支撑滑块、支撑气缸、截断模容腔、截断块、定位导杆、定位滑套、脱料气缸、脱料顶板构成;下模座的上方设置上模座,所述的下模座的上侧面中部从左到右依次设置冲形底模、第一支撑模和第二支撑模,所述的上模座的下侧面中部从左到右依次设置冲形顶模、第一折弯模和第二折弯模,所述的冲形底模、第一支撑模和第二支撑模的上端面位于同一水平面,所述的冲形顶模与冲形底模相互扣合,第一支撑模和第一折弯模相互扣合,第二折弯模和第二支撑模相互扣合,所述的第一折弯模的一侧设置脱料机构;In order to achieve the above object, the present invention adopts the following technical scheme: a method for operating a three-wheeled motorcycle edge cover continuous three-step stamping die device, the described three-wheel motorcycle edge cover continuous three-step stamping die device, It is composed of: lower mold base, upper mold base, punching bottom mold, first supporting mold, second supporting mold, punching top mold, first bending mold, second bending mold, top mold cavity, forming part , outer convex part, slide rail, support slider, support cylinder, truncated mold cavity, truncated block, positioning guide rod, positioning sliding sleeve, stripping cylinder, and stripping top plate; the upper mold base is set above the lower mold base, The middle part of the upper side of the lower mold base is provided with a punching bottom mold, the first supporting mold and the second supporting mold in sequence from left to right, and the middle part of the lower side of the upper mold base is provided with a punching top in turn from left to right. mold, the first bending die and the second bending die, the upper end surfaces of the punching bottom die, the first supporting die and the second supporting die are located on the same horizontal plane, and the punching top die and the punching bottom die Buckling with each other, the first support mold and the first bending mold are buckled with each other, the second bending mold and the second support mold are buckled with each other, and a stripping mechanism is set on one side of the first bending mold;
使用时,将下模座水平固定,将上模座的顶部与液压缸的活塞端固定,将金属板材的前端部覆盖在冲形底模的上侧面,通过液压缸控制上模座与下模座扣合后,金属板材的前侧被冲压出所需形状,使上模座抬起,将金属板材的前端部向右推进,使金属板材的前端部覆盖在第一支撑模的上侧面上,控制上模座与下模座扣合,第一折弯模和第一支撑模对成形后金属板材的边缘部两侧进行九十度折弯,折弯的同时,冲形底模与冲形顶模之间的金属板材被冲压成形,控制上模座抬起,重复将金属板材向右推进,使金属板材的前端部覆盖在第二折弯模上,控制上模座与下模座扣合,第二支撑模和第一折弯模对经过第一之支撑模和第一折弯模折弯后的金属板材的中部两侧进行折弯,并包裹在第二支撑模外周,形成包边套,同时,截断模和截断模容腔扣合,使得包裹在第二支撑模外周的包边套脱离金属板材,第一支撑模和第一折弯模对冲压成形后的金属板材的边缘部两侧进行折弯,同时,冲形顶模和冲形底模将与其对应的金属板材进行冲压成形,控制上模座抬起,启动支撑气缸,支撑气缸将支撑滑块沿滑轨向后拉动,使其位于第二支撑模的后侧,启动脱料气缸,脱料气缸将脱料顶板向后推动,脱料顶板带动包裹在第二支撑模上的包边套脱离第二支撑模,通过支撑气缸控制支撑滑块沿滑轨向前滑动,使其位于第二支撑模的下侧,对第二支撑模进行支撑,重复向右侧推动金属板,持续进行成形、折弯、和退料操作,直至完成所有生产任务。When in use, fix the lower mold base horizontally, fix the top of the upper mold base with the piston end of the hydraulic cylinder, cover the front end of the metal plate on the upper side of the punching bottom mold, and control the upper mold base and the lower mold through the hydraulic cylinder After the seat is fastened, the front side of the metal sheet is punched out into the required shape, the upper mold base is lifted, and the front end of the metal sheet is pushed to the right, so that the front end of the metal sheet covers the upper side of the first support mold , control the fastening of the upper die base and the lower die base, the first bending die and the first support die perform ninety-degree bending on both sides of the edge of the formed metal sheet, and at the same time of bending, the punching bottom die and the punching die The metal sheet between the top dies is stamped and formed, and the upper die base is controlled to lift up, and the metal sheet is repeatedly pushed to the right, so that the front end of the metal sheet covers the second bending die, and the upper die base and the lower die base are controlled Buckle together, the second support mold and the first bending mold bend the two sides of the middle part of the metal sheet bent by the first support mold and the first bending mold, and wrap it around the outer periphery of the second support mold to form At the same time, the truncated mold and the cavity of the truncated mold are fastened together, so that the hemmed sleeve wrapped around the outer periphery of the second support mold is separated from the metal sheet, and the first support mold and the first bending mold are pressed against the sheet metal after stamping. Bending is carried out on both sides of the edge. At the same time, the punching top die and the punching bottom die will press and form the corresponding metal sheet, control the lifting of the upper die base, start the supporting cylinder, and the supporting cylinder will support the slider along the slide rail. Pull back to make it located on the back side of the second support mold, start the stripping cylinder, the stripping cylinder pushes the stripping top plate backward, and the stripping top plate drives the hemming sleeve wrapped on the second support mold to separate from the second support mold , through the support cylinder to control the support slider to slide forward along the slide rail, so that it is located on the lower side of the second support mold, support the second support mold, repeatedly push the metal plate to the right, and continue forming, bending, and Material return operations until all production tasks are completed.
所述的冲形底模为四方形,冲形底模的前后两侧设置为顶模容腔,前后两侧的顶模容腔之间所对应部分构成成形部,所述的顶模容腔与冲形顶模的外凸部相互扣合。The punching bottom mold is square, and the front and rear sides of the punching bottom mold are set as top mold cavities, and the corresponding parts between the top mold cavities on the front and rear sides form a forming part, and the top mold cavity Interlocking with the convex part of the punching top die.
所述的第一支撑模为四方形,第一折弯模的截面为倒凹形,第一支撑模与第一折弯模的内凹部相互扣合。The first supporting mold is square, the cross section of the first bending mold is concave, and the first supporting mold and the inner concave part of the first bending mold are interlocked.
所述的第一支撑模的右端部的上侧设置卡槽,所述的第二折弯模的左端设置于卡槽内。A slot is provided on the upper side of the right end of the first supporting die, and the left end of the second bending die is disposed in the slot.
所述的第二支撑模为四方形,第二折弯模的截面为倒凹形,第二折弯模的宽度小于第一折弯模的宽度,第二支撑模的与第二折弯模的内凹部相互扣合。The second supporting mold is square, the cross-section of the second bending mold is concave, the width of the second bending mold is smaller than the width of the first bending mold, the second supporting mold and the second bending mold The inner recesses of the two are fastened together.
所述的第二支撑模的右端部所对应的下模座的上侧面设置滑轨,滑轨上滑动设置支撑滑块,滑轨的后方设置支撑气缸,支撑滑块上的上端面与第二支撑模的下侧面滑动配合,支撑滑块的后端与支撑气缸的活塞端固定连接。The upper side of the lower mold base corresponding to the right end of the second support mold is provided with a slide rail, a support slider is slidably arranged on the slide rail, and a support cylinder is arranged behind the slide rail, and the upper end surface on the support slider is in contact with the second The lower side of the support mold is slidably fitted, and the rear end of the support slide is fixedly connected with the piston end of the support cylinder.
所述的第二支撑模的左端部设置截断模容腔,截断模容腔所对应的上模座的下侧,设置截断块,所述的截断块与截断模容腔相互扣合。The left end of the second support mold is provided with a truncated mold cavity, and the lower side of the upper mold base corresponding to the truncated mold cavity is provided with a truncated block, and the truncated block and the truncated mold cavity are interlocked.
所述的下模座的上侧面的前侧边缘和后侧边缘均设置一对定位导杆,每个定位导杆所对应的上模座的下侧面均固定设置定位滑套。A pair of positioning guide rods are arranged on the front side edge and the rear side edge of the upper side of the upper die base, and a positioning sliding sleeve is fixedly installed on the lower side of the upper die base corresponding to each positioning guide rod.
所述的脱料机构的结构为:第一折弯模的一侧横向设置脱料气缸,脱料气缸的活塞端设置脱料顶板,脱料顶板与第二支撑模的相向面互相贴合。本发明的有益效果是:本发明结构简单、使用方便,能够通过上模座和下模座的扣合,同步完成金属板材的冲压成形、第一次折弯和第二次折弯三步冲压工序, 在制成包边套后,能够通过退料气缸和退料顶板使制成的包边套脱离冲压模具,无需工人过多干预,有效的保障了各道工序的连续形,能够大幅度提高生产效率、节省工人体力和用工数量、有降低生产成本,有效的解决了目前在对三轮摩托车包边套冲压制作时,每次冲压都需要在不同的冲压模具上进行导致的操作繁琐、生产效率低下的问题,适合普遍推广使用。The structure of the stripping mechanism is as follows: a stripping cylinder is arranged laterally on one side of the first bending die, and a stripping top plate is arranged at the piston end of the stripping cylinder, and the stripping top plate and the opposite surface of the second supporting mold are attached to each other. The beneficial effects of the present invention are: the present invention is simple in structure and easy to use, and can synchronously complete the three-step stamping of metal plate stamping, first bending and second bending through the fastening of the upper mold base and the lower mold base process, after the hemming sleeve is made, the finished hemming sleeve can be separated from the stamping die through the material return cylinder and the material return top plate, without too much intervention by workers, which effectively guarantees the continuous shape of each process, and can be greatly improved. Improve production efficiency, save workers' physical strength and labor quantity, reduce production costs, and effectively solve the cumbersome operation caused by the need for each stamping to be carried out on different stamping dies when stamping the three-wheeled motorcycle edge cover. , The problem of low production efficiency is suitable for general promotion and use.
附图说明Description of drawings
下面结合附图对本发明作进一步说明:The present invention will be further described below in conjunction with accompanying drawing:
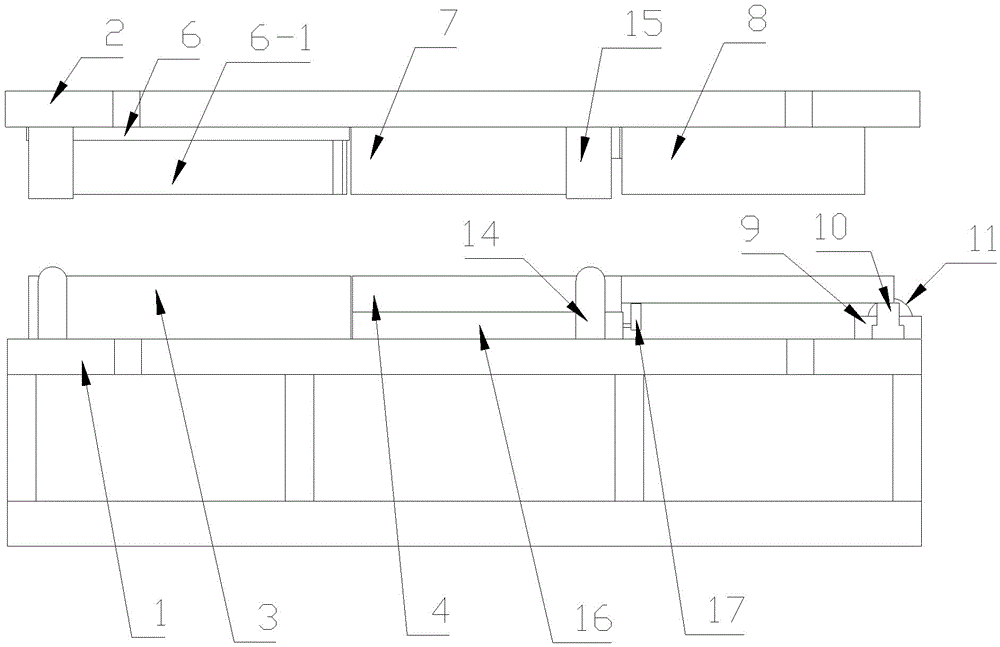
图1是本发明的总装结构示意图;Fig. 1 is a schematic diagram of the assembly structure of the present invention;
图2是本发明下模座的俯视结构示意图;Fig. 2 is a top view structural schematic diagram of the lower mold base of the present invention;
图3是本发明上模座的仰视结构示意图;Fig. 3 is a schematic view of the structure of the upper mold base of the present invention;
图4是本发明下模座的立体结构示意图;Fig. 4 is a three-dimensional structural schematic view of the lower mold base of the present invention;
图5是本发明上模座的立体结构示意图;Fig. 5 is the schematic diagram of the three-dimensional structure of the upper mold base of the present invention;
图中:下模座1、上模座2、冲形底模3、第一支撑模4、第二支撑模5、冲形顶模6、第一折弯模7、第二折弯模8、顶模容腔3-1、成形部3-2、外凸部6-1、滑轨9、支撑滑块10、支撑气缸11、截断模容腔12、截断块13、定位导杆14、定位滑套15、脱料气缸16、脱料顶板17。In the figure:
具体实施方式Detailed ways
下面结合附图与具体实施方式对本发明作进一步详细说明:Below in conjunction with accompanying drawing and specific embodiment the present invention is described in further detail:
实施例1Example 1
下模座1的上方设置上模座2,所述的下模座1的上侧面中部从左到右依次设置冲形底模3、第一支撑模4和第二支撑模5,所述的上模座2的下侧面中部从左到右依次设置冲形顶模6、第一折弯模7和第二折弯模8,所述的冲形底模3、第一支撑模4和第二支撑模5的上端面位于同一水平面,所述的冲形顶模6与冲形底模3相互扣合,第一支撑模4和第一折弯模7相互扣合,第二折弯模8和第二支撑模5相互扣合,所述的第一折弯模7的一侧设置脱料机构;The top of the
使用时,将下模座1水平固定,将上模座2的顶部与液压缸的活塞端固定,将金属板材的前端部覆盖在冲形底模3的上侧面,通过液压缸控制上模座2与下模座1扣合后,金属板材的前侧被冲压出所需形状,使上模座2抬起,将金属板材的前端部向右推进,使金属板材的前端部覆盖在第一支撑模4的上侧面上,控制上模座2与下模座1扣合,第一折弯模7和第一支撑模4对成形后金属板材的边缘部两侧进行九十度折弯,折弯的同时,冲形底模3与冲形顶模6之间的金属板材被冲压成形,控制上模座2抬起,重复将金属板材向右推进,使金属板材的前端部覆盖在第二折弯模8上,控制上模座2与下模座1扣合,第二支撑模5和第一折弯模7对经过第一之支撑模和第一折弯模7折弯后的金属板材的中部两侧进行折弯,并包裹在第二支撑模5外周,形成包边套,同时,截断模和截断模容腔12扣合,使得包裹在第二支撑模5外周的包边套脱离金属板材,第一支撑模4和第一折弯模7对冲压成形后的金属板材的边缘部两侧进行折弯,同时,冲形顶模6和冲形底模3将与其对应的金属板材进行冲压成形,控制上模座2抬起,启动支撑气缸11,支撑气缸11将支撑滑块10沿滑轨9向后拉动,使其位于第二支撑模4的后侧,启动脱料气缸16,脱料气缸16将脱料顶板17向后推动,脱料顶板17带动包裹在第二支撑模4上的包边套脱离第二支撑模4,通过支撑气缸11控制支撑滑块10沿滑轨9向前滑动,使其位于第二支撑模4的下侧,对第二支撑模4进行支撑,重复向右侧推动金属板,持续进行成形、折弯、和退料操作,直至完成所有生产任务。When in use, fix the
实施例2Example 2
所述的冲形底模3为四方形,冲形底模3的前后两侧设置为顶模容腔3-1,前后两侧的顶模容腔3-1之间所对应部分构成成形部3-2,所述的顶模容腔3-1与冲形顶模6的外凸部6-1相互扣合。The punching
实施例3Example 3
所述的第一支撑模4为四方形,第一折弯模7的截面为倒凹形,第一支撑模4与第一折弯模7的内凹部相互扣合。The first supporting
实施例4Example 4
所述的第一支撑模4的右端部的上侧设置卡槽,所述的第二折弯模8的左端设置于卡槽内。A slot is provided on the upper side of the right end of the first supporting
实施例5Example 5
所述的第二支撑模5为四方形,第二折弯模8的截面为倒凹形,第二折弯模8的宽度小于第一折弯模7的宽度,第二支撑模5的与第二折弯模8的内凹部相互扣合。The
实施例6Example 6
所述的第二支撑模5的右端部所对应的下模座1的上侧面设置滑轨9,滑轨9上滑动设置支撑滑块10,滑轨9的后方设置支撑气缸11,支撑滑块10上的上端面与第二支撑模5的下侧面滑动配合,支撑滑块10的后端与支撑气缸11的活塞端固定连接。The upper side of the
实施例7Example 7
所述的第二支撑模5的左端部设置截断模容腔12,截断模容腔12所对应的上模座2的下侧,设置截断块13,所述的截断块13与截断模容腔12相互扣合。The left end portion of described
实施例8Example 8
所述的下模座1的上侧面的前侧边缘和后侧边缘均设置一对定位导杆14,每个定位导杆14所对应的上模座2的下侧面均固定设置定位滑套15。A pair of
实施例9Example 9
所述的脱料机构的结构为:第一折弯模7的一侧横向设置脱料气缸16,脱料气缸16的活塞端设置脱料顶板17,脱料顶板17与第二支撑模5的相向面互相贴合。The structure of the stripping mechanism is as follows: one side of the
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310086058.1A CN116213527B (en) | 2023-02-09 | 2023-02-09 | An operating method for a continuous three-step stamping die device for a three-wheeled motorcycle hemming sleeve |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310086058.1A CN116213527B (en) | 2023-02-09 | 2023-02-09 | An operating method for a continuous three-step stamping die device for a three-wheeled motorcycle hemming sleeve |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN116213527A true CN116213527A (en) | 2023-06-06 |
| CN116213527B CN116213527B (en) | 2025-10-03 |
Family
ID=86578048
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310086058.1A Active CN116213527B (en) | 2023-02-09 | 2023-02-09 | An operating method for a continuous three-step stamping die device for a three-wheeled motorcycle hemming sleeve |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116213527B (en) |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN210333867U (en) * | 2019-08-02 | 2020-04-17 | 苏州恒全鑫五金科技有限公司 | Bending die for high-bending product |
| CN216989507U (en) * | 2021-09-18 | 2022-07-19 | 苏州市诺弗电器有限公司 | Stamping die convenient to drawing of patterns |
| CN218079974U (en) * | 2022-08-03 | 2022-12-20 | 东莞市旺都模具有限公司 | Novel car hardware stamping die |
| CN219616509U (en) * | 2023-02-09 | 2023-09-01 | 河南金彭车业有限公司 | Continuous three-step stamping die device for motor tricycle edging sleeve |
-
2023
- 2023-02-09 CN CN202310086058.1A patent/CN116213527B/en active Active
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN210333867U (en) * | 2019-08-02 | 2020-04-17 | 苏州恒全鑫五金科技有限公司 | Bending die for high-bending product |
| CN216989507U (en) * | 2021-09-18 | 2022-07-19 | 苏州市诺弗电器有限公司 | Stamping die convenient to drawing of patterns |
| CN218079974U (en) * | 2022-08-03 | 2022-12-20 | 东莞市旺都模具有限公司 | Novel car hardware stamping die |
| CN219616509U (en) * | 2023-02-09 | 2023-09-01 | 河南金彭车业有限公司 | Continuous three-step stamping die device for motor tricycle edging sleeve |
Also Published As
| Publication number | Publication date |
|---|---|
| CN116213527B (en) | 2025-10-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102699217B (en) | Device for rounding and slotting housing of water heater | |
| CN207288617U (en) | Two folding mould of one-pass molding | |
| CN219616509U (en) | Continuous three-step stamping die device for motor tricycle edging sleeve | |
| CN109622765A (en) | A kind of pipe fitting flattening mold | |
| CN102921802A (en) | Method for forming car rear shaft support assembly cross beam | |
| US7237423B1 (en) | Apparatus for stretch forming blanks | |
| CN103357757A (en) | Trimming and punching die for processing quarter window reinforcing plate on automobile | |
| CN116213527B (en) | An operating method for a continuous three-step stamping die device for a three-wheeled motorcycle hemming sleeve | |
| CN102825132A (en) | Stamping Technology and Stamping Die of Freezer Handle | |
| CN106077376A (en) | Automatic forming equipment | |
| CN211588260U (en) | Flanging forming die for automobile side wall outer plate | |
| CN204182827U (en) | A kind of bender shaping for doorframe band iron curved arc | |
| CN202725834U (en) | Freezer handle stamping die | |
| CN217831520U (en) | Metal plate forming bending machine die | |
| CN112620490B (en) | A progressive blanking die for a side panel front inner panel reinforcement plate | |
| CN214639588U (en) | Progressive blanking forming die for rear cross beam of car roof | |
| CN209647377U (en) | The blanking cover product integral type progressive die rises type molding structure on a kind of automobile air conditioning heater | |
| CN212442723U (en) | Automatic metal plate bending device | |
| CN205309117U (en) | Drawing die of car front longitudinal | |
| CN213043015U (en) | Lug arc forming die | |
| CN104624807B (en) | A kind of alligator clamp progressive die with bolster | |
| CN213052365U (en) | Multi-station automatic stamping forming die for metal pipes | |
| CN221109612U (en) | Stamping die for front coaming assembly | |
| CN103495666B (en) | Spring clamp progressive die | |
| CN211218305U (en) | Material returning mechanism of pneumatic cylinder of side shaping die |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |