CN114919140A - Mould for machining router shell based on inner and outer sliding block core-pulling mechanism - Google Patents
Mould for machining router shell based on inner and outer sliding block core-pulling mechanism Download PDFInfo
- Publication number
- CN114919140A CN114919140A CN202210687218.3A CN202210687218A CN114919140A CN 114919140 A CN114919140 A CN 114919140A CN 202210687218 A CN202210687218 A CN 202210687218A CN 114919140 A CN114919140 A CN 114919140A
- Authority
- CN
- China
- Prior art keywords
- slider
- mold
- bending part
- core
- router
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images





Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/40—Removing or ejecting moulded articles
- B29C45/44—Removing or ejecting moulded articles for undercut articles
- B29C45/4435—Removing or ejecting moulded articles for undercut articles using inclined, tiltable or flexible undercut forming elements driven by the ejector means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/26—Moulds
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/26—Moulds
- B29C45/33—Moulds having transversely, e.g. radially, movable mould parts
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02D—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN INFORMATION AND COMMUNICATION TECHNOLOGIES [ICT], I.E. INFORMATION AND COMMUNICATION TECHNOLOGIES AIMING AT THE REDUCTION OF THEIR OWN ENERGY USE
- Y02D30/00—Reducing energy consumption in communication networks
- Y02D30/70—Reducing energy consumption in communication networks in wireless communication networks
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
Abstract
本申请涉及注塑模具成型领域,提供一种基于内外滑块抽芯机构加工路由器外壳的模具,包括:外滑块、内滑块、滑块锁紧块、动模和定模;滑块锁紧块包括第一弯折部和第二弯折部,合模时,第一弯折部插入外滑块,第二弯折部插入内滑块,脱模时,外滑块朝远离定模的方向移动,内滑块朝靠近动模中心的方向移动。由于脱模时,优先释放散热孔和接线孔处对应的内滑块和外滑块,导致加工的路由器外壳的散热孔抱紧力优先释放和接线孔处的滑块开模前抽出保证正常开模,进而整个路由器外壳几乎无抱紧力,进而避免脱模时外壳会向模具一侧移动,划伤加工的路由器的外壳。
The application relates to the field of injection mold molding, and provides a mold for processing a router casing based on an inner and outer slider core-pulling mechanism, including: an outer slider, an inner slider, a slider locking block, a movable mold and a fixed mold; The block includes a first bending part and a second bending part. When the mold is closed, the first bending part is inserted into the outer sliding block, and the second bending part is inserted into the inner sliding block. When demolding, the outer sliding block faces away from the fixed mold. direction, the inner slider moves toward the direction close to the center of the movable mold. When demoulding, the inner and outer sliders corresponding to the heat dissipation holes and wiring holes are preferentially released, resulting in the preferential release of the clamping force of the heat dissipation holes of the processed router shell and the slider at the wiring holes being pulled out before mold opening to ensure normal opening. mold, and the entire router shell has almost no holding force, thus avoiding that the shell will move to the side of the mold when demoulding, and scratch the shell of the processed router.
Description
技术领域technical field
本申请涉及注塑模具成型领域,尤其涉及一种基于内外滑块抽芯机构加工路由器外壳的模具。The application relates to the field of injection mold molding, and in particular, to a mold for processing a router shell based on an inner and outer slider core-pulling mechanism.
背景技术Background technique
随着信息化时代的到来,万物互联已经成为大的行业发展趋势。其中,无线信号传输的重要程度及受关注度越来越高,无线产品按功率分很多种,最常见的是家用路由器和商用路由器。With the advent of the information age, the Internet of Everything has become a major industry development trend. Among them, the importance and attention of wireless signal transmission are getting higher and higher. There are many types of wireless products according to power, and the most common ones are home routers and commercial routers.
随着对无线信号质量要求的增高,因此路由器功率的增加,从而路由器产生更多的热量,集中在路由器里面,为了对路由器散热,路由器外壳的侧面会设置有散热孔,便于散热,另外出于安全的考虑,散热孔的大小会受到行业规范限制(目前大约在0.8mm),在不能加大孔直径的情况下,散热孔的设计就变得尤为重要。As the requirements for wireless signal quality increase, the power of the router increases, so that the router generates more heat, which is concentrated in the router. In order to dissipate heat from the router, there are cooling holes on the side of the router shell to facilitate heat dissipation. For safety reasons, the size of the heat dissipation hole will be limited by the industry standard (currently about 0.8mm). When the diameter of the hole cannot be increased, the design of the heat dissipation hole becomes particularly important.
路由器的散热孔和接线接口设计在同一侧,而且两个孔相距间隙只有一个产品壁厚度,其中接线接口向外输出接线,散热孔热量从内部向外释放,散热孔的角度方向内大外小,这样就和接线孔两个方向正好相反。The cooling holes and the wiring interface of the router are designed on the same side, and the gap between the two holes is only one product wall thickness. The wiring interface outputs the wiring to the outside, and the heat of the cooling holes is released from the inside to the outside. The angle of the cooling holes is large inside and small outside. , so that the two directions of the wiring holes are exactly opposite.
在实际生产中,为了加工此类路由器的外壳,需要用到模具,外壳的侧面设置孔,在对应模具上就成了倒扣部分,而由于路由器本身不对称,散热孔和接线孔位置因为有孔,抱紧力大,又由于散热孔和接线孔的对立面是平的(没有孔),没有抱紧力,因此路由器外壳对模具的抱紧力有差别,导致脱模时外壳会向模具一侧移动(抱紧力大的一侧),从而会划伤加工的路由器的外壳。In actual production, in order to process the casing of this type of router, a mold is needed. The side of the casing is provided with a hole, which becomes an undercut part on the corresponding mold. Due to the asymmetry of the router itself, the position of the heat dissipation hole and the wiring hole is due to the The hole has a large holding force, and because the opposite sides of the heat dissipation hole and the wiring hole are flat (no holes), there is no holding force, so the holding force of the router shell to the mold is different, resulting in the shell will be removed from the mold. side movement (the side that holds the most force), which will scratch the casing of the machined router.
发明内容SUMMARY OF THE INVENTION
本申请旨在提供一种基于内外滑块抽芯机构加工路由器外壳的模具,以解决使用模具加工路由器的外壳,在脱模时外壳会向模具一侧移动,划伤外壳的技术问题。The purpose of the present application is to provide a mold for processing the router shell based on the inner and outer slider core-pulling mechanism, so as to solve the technical problem of using the mold to process the router shell, the shell will move to the side of the mold when demoulding, and the shell will be scratched.
本申请提供一种基于内外滑块抽芯机构加工路由器外壳的模具,包括:外滑块、内滑块、滑块锁紧块、动模和定模。The present application provides a mold for processing a router casing based on an inner and outer slider core-pulling mechanism, including: an outer slider, an inner slider, a slider locking block, a movable mold and a fixed mold.
所述外滑块与所述定模侧面活动连接,所述内滑块与所述动模侧面活动连接,所述定模上设置有定模背板,所述滑块锁紧块固定在所述定模背板上,所述外滑块、内滑块和滑块锁紧块位于同一侧。The outer sliding block is movably connected with the side of the fixed mold, the inner sliding block is movably connected with the side of the movable mold, the fixed mold is provided with a fixed mold back plate, and the sliding block locking block is fixed on the fixed mold. On the backboard of the fixed die, the outer sliding block, the inner sliding block and the sliding block locking block are located on the same side.
所述滑块锁紧块包括第一弯折部和第二弯折部,合模时,所述第一弯折部插入所述外滑块,所述第一弯折部与所述外滑块接触,所述第二弯折部插入所述内滑块,所述第二弯折部与所述内滑块接触。The slider locking block includes a first bending part and a second bending part. When the mold is closed, the first bending part is inserted into the outer slider, and the first bending part is connected with the outer sliding part. The second bent portion is inserted into the inner slider, and the second bent portion is in contact with the inner slider.
所述第一弯折部和第二弯折部一体成型,所述第一弯折部和第二弯折部之间夹角为钝角,所述第一弯折部和第二弯折部连接处向远离所述动模方向弯折,以使脱模时,所述外滑块朝远离所述定模的方向移动,所述内滑块朝靠近所述动模的方向移动。The first bending part and the second bending part are integrally formed, the included angle between the first bending part and the second bending part is an obtuse angle, and the first bending part and the second bending part are connected The part is bent in a direction away from the movable mold, so that when demolding, the outer slider moves in a direction away from the fixed mold, and the inner slider moves in a direction close to the movable mold.
可选的,所述外滑块包括:外滑块本体、斜销孔和外孔抽芯,所述斜销孔和外孔抽芯设置在所述外滑块本体上,所述斜销孔的朝向与第一弯折部的朝向一致,合模时,所述滑块锁紧块插入所述斜销孔。Optionally, the outer slider includes: an outer slider body, an oblique pin hole and an outer hole core pulling, the oblique pin hole and the outer hole core pulling are arranged on the outer slider body, and the oblique pin hole is The orientation of the first bending part is consistent with the orientation of the first bending part. When the mold is closed, the slider locking block is inserted into the oblique pin hole.
可选的,所述外孔抽芯形状为棱柱或圆柱体,所述外孔抽芯用于成型路由器外壳上的接线孔。Optionally, the shape of the outer hole core-pulling is a prism or a cylinder, and the outer hole core-pulling is used to form a wiring hole on the outer casing of the router.
可选的,所述内滑块包括:内滑块本体、斜销拉槽和内孔抽芯,所述斜销拉槽和内孔抽芯设置在所述内滑块本体上,所述斜销拉槽的朝向与第二弯折部朝向一致,合模时,所述滑块锁紧块插入所述斜销拉槽。Optionally, the inner slider includes: an inner slider body, an oblique pin pulling groove and an inner hole core pulling, the oblique pin pulling groove and the inner hole core pulling are arranged on the inner slider body, and the oblique pin pulling groove and the inner hole core pulling are arranged on the inner slider body. The orientation of the pin pulling slot is consistent with the orientation of the second bending portion, and the slider locking block is inserted into the oblique pin pulling slot when the mold is closed.
可选的,所述内孔抽芯为多个片状凸起,所述内孔抽芯用于成型路由器外壳上的散热孔。Optionally, the inner-hole core-pulling is a plurality of sheet-like protrusions, and the inner-hole core-pulling is used to form the heat dissipation holes on the router casing.
可选的,所述外滑块与所述定模侧面通过压片活动连接。Optionally, the outer sliding block and the side surface of the fixed mold are movably connected through tablet pressing.
可选的,所述内滑块与所述动模侧面通过压片活动连接。Optionally, the inner sliding block and the side surface of the movable mold are movably connected through tablet pressing.
可选的,所述外滑块的材料为:冷作模具钢SKD11、NAK80或S136。Optionally, the material of the outer slider is: cold work die steel SKD11, NAK80 or S136.
可选的,所述内滑块的材料为:冷作模具钢SKD11、NAK80或S136。Optionally, the material of the inner slider is: cold work die steel SKD11, NAK80 or S136.
可选的,所述滑块锁紧块的材料为:冷作模具钢SKD11、NAK80或S136。Optionally, the material of the slider locking block is: cold work die steel SKD11, NAK80 or S136.
由以上技术方案可知,本申请提供一种基于内外滑块抽芯机构加工路由器外壳的模具,包括:外滑块、内滑块、滑块锁紧块、动模和定模;所述外滑块与所述定模侧面活动连接,所述内滑块与所述动模侧面活动连接,所述定模上设置有定模背板,所述滑块锁紧块固定在所述定模背板上,所述外滑块、内滑块和滑块锁紧块位于同一侧;所述滑块锁紧块包括第一弯折部和第二弯折部,合模时,所述第一弯折部插入所述外滑块,所述第一弯折部与所述外滑块接触,所述第二弯折部插入所述内滑块,所述第二弯折部与所述内滑块接触;所述第一弯折部和第二弯折部一体成型,所述第一弯折部和第二弯折部之间夹角为钝角,所述第一弯折部和第二弯折部连接处向远离所述动模方向弯折,以使脱模时,所述外滑块朝远离所述定模的方向移动,所述内滑块朝靠近所述动模的方向移动。It can be seen from the above technical solutions that the present application provides a mold for processing a router casing based on an inner and outer slider core-pulling mechanism, including: an outer slider, an inner slider, a slider locking block, a movable mold and a fixed mold; The block is movably connected to the side of the fixed mold, the inner slider is movably connected to the side of the movable mold, the fixed mold is provided with a fixed mold back plate, and the slider locking block is fixed on the fixed mold back On the plate, the outer slider, the inner slider and the slider locking block are located on the same side; the slider locking block includes a first bending part and a second bending part, when the mold is closed, the first bending part The bent portion is inserted into the outer slider, the first bent portion is in contact with the outer slider, the second bent portion is inserted into the inner slider, and the second bent portion is in contact with the inner slider. The slider is in contact; the first bending part and the second bending part are integrally formed, the angle between the first bending part and the second bending part is an obtuse angle, and the first bending part and the second bending part are The connecting part of the bending part is bent in a direction away from the movable mold, so that when demolding, the outer slider moves away from the fixed mold, and the inner slider moves toward the movable mold .
在实际应用中,本申请提供的一种基于内外滑块抽芯机构加工路由器外壳的模具,使用时,合模时动模与定模紧贴,滑块锁紧块的第一弯折部插入外滑块,第一弯折部与外滑块接触,滑块锁紧块的第二弯折部插入内滑块,第二弯折部与内滑块接触;脱模时,定模上的定模背板先分开,带动滑块锁紧块从外滑块和内滑块内拔出,外滑块朝远离定模的方向移动,内滑块朝靠近所述动模的方向移动,待散热孔和接线孔脱模后,再从模具中顶出整个路由器外壳,脱模完成。由于在脱模时,优先松开散热孔和接线孔处对应的内滑块和外滑块,导致加工的路由器外壳的散热孔和接线孔处的抱紧力减小,进而整个路由器外壳几乎无抱紧力,进而避免脱模时外壳会向模具一侧移动,划伤加工的路由器的外壳。In practical applications, the present application provides a mold for processing router casings based on an inner and outer slider core-pulling mechanism. When in use, the movable mold and the fixed mold are in close contact when the mold is closed, and the first bent portion of the slider locking block is inserted into the mold. The outer slider, the first bending part is in contact with the outer slider, the second bending part of the slider locking block is inserted into the inner slider, and the second bending part is in contact with the inner slider; The back plate of the fixed mold is first separated, and the slider locking block is pulled out from the outer slider and the inner slider, the outer slider moves away from the fixed mold, and the inner slider moves toward the moving mold. After the heat dissipation holes and wiring holes are demolded, the entire router shell is ejected from the mold, and the demoulding is completed. Since the inner and outer sliders corresponding to the heat dissipation holes and the wiring holes are preferentially loosened during demoulding, the tightening force at the heat dissipation holes and the wiring holes of the processed router shell is reduced, and the entire router shell is almost free of Hold tight to prevent the shell from moving to the side of the mold when demolding, and scratch the shell of the router.
附图说明Description of drawings
为了更清楚地说明本申请的技术方案,下面将对实施例中所需要使用的附图作简单地介绍,显而易见地,对于本领域普通技术人员而言,在不付出创造性劳动的前提下,还可以根据这些附图获得其他的附图。In order to illustrate the technical solutions of the present application more clearly, the accompanying drawings required in the embodiments will be briefly introduced below. Obviously, for those of ordinary skill in the art, without creative work, the Additional drawings can be obtained from these drawings.
图1为外滑块在定模上的结构示意图;Figure 1 is a schematic diagram of the structure of the outer slider on the fixed die;
图2为内滑块在动模上的结构示意图;Figure 2 is a schematic diagram of the structure of the inner slider on the movable die;
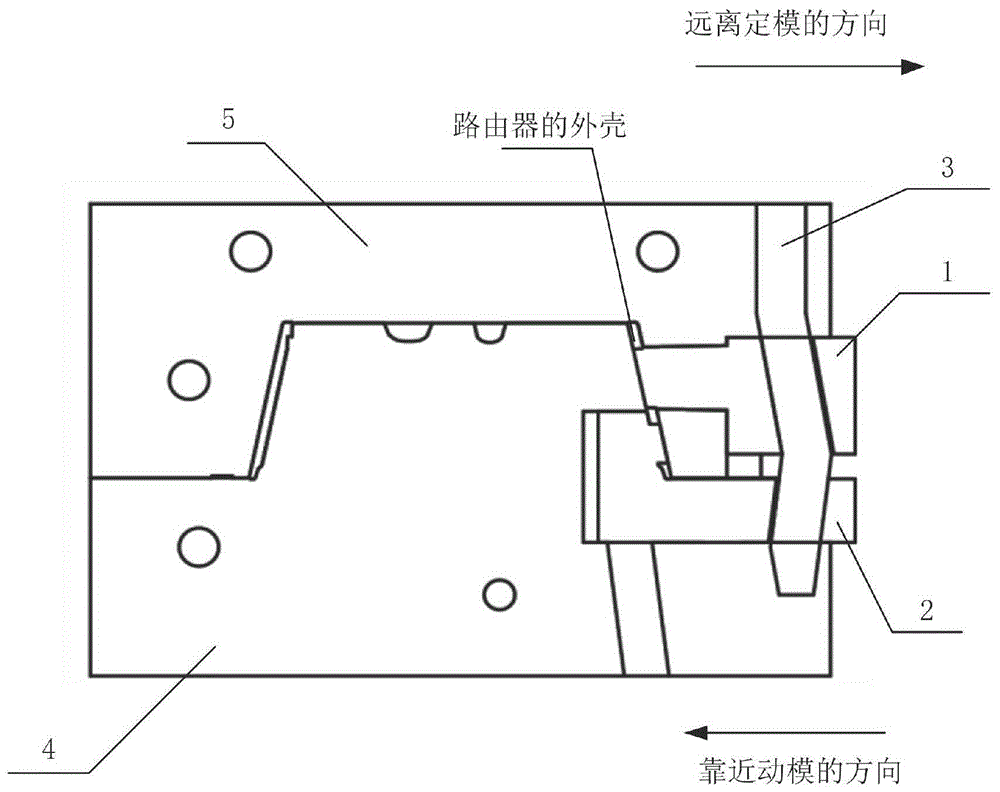
图3为本申请实施例提供的基于内外滑块抽芯机构加工路由器外壳的模具在合模时的正视图;3 is a front view of a mold for processing a router casing based on an inner and outer slider core-pulling mechanism provided by an embodiment of the application when the mold is closed;
图4为抽芯机构的放大图;Figure 4 is an enlarged view of the core pulling mechanism;
图5为外滑块结构示意图;Figure 5 is a schematic diagram of the structure of the outer slider;
图6为内滑块结构示意图;Figure 6 is a schematic diagram of the structure of the inner slider;
图7为在脱模时,抽芯机构中外滑块、内滑块和滑块锁紧块的移动方向示意图;Figure 7 is a schematic diagram of the moving direction of the outer slider, the inner slider and the slider locking block in the core pulling mechanism during demolding;
图8为本申请实施例提供的基于内外滑块抽芯机构加工路由器外壳的模具在脱模时的正视图。FIG. 8 is a front view of the mold for processing the router casing based on the inner and outer slider core-pulling mechanism provided by the embodiment of the present application when the mold is demolded.
图中:In the picture:
1-外滑块,11-外滑块主体,12-斜销孔,13-外孔抽芯,2-内滑块,21-内滑块本体,22-斜销拉槽,23-内孔抽芯,3-滑块锁紧块,31-第一弯折部,32-第二弯折部,4-动模,5-定模,51-定模背板,6-压片。1-outer slider, 11-outer slider body, 12-oblique pin hole, 13-outer hole core pulling, 2-inner slider, 21-inner slider body, 22- oblique pin slot, 23-inner hole Core pulling, 3-slide block locking block, 31-first bending part, 32-second bending part, 4-movable mold, 5-fixed mold, 51-fixed mold back plate, 6-tablet.
具体实施方式Detailed ways
下面将结合本申请实施例中的附图,对本申请实施例中的技术方案进行完整、清楚的描述。显然,所描述的实施例仅仅是本申请一部分实施例,而不是全部的实施例。基于本申请中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本申请保护的范围。The technical solutions in the embodiments of the present application will be described completely and clearly below with reference to the accompanying drawings in the embodiments of the present application. Obviously, the described embodiments are only a part of the embodiments of the present application, but not all of the embodiments. Based on the embodiments in the present application, all other embodiments obtained by those of ordinary skill in the art without creative efforts shall fall within the protection scope of the present application.
参见图1为外滑块在定模上的结构示意图;参见图2为内滑块在动模上的结构示意图;参见图3为本申请实施例提供的基于内外滑块抽芯机构加工路由器外壳的模具在合模时的正视图;参见图4为抽芯机构的放大图;参见图7为在脱模时,抽芯机构中外滑块、内滑块和滑块锁紧块的移动方向示意图,参见图8为本申请实施例提供的基于内外滑块抽芯机构加工路由器外壳的模具在脱模时的正视图。Referring to FIG. 1, it is a schematic structural diagram of an outer slider on a fixed mold; referring to FIG. 2, it is a schematic structural diagram of an inner slider on a movable mold; referring to FIG. The front view of the mold when the mold is closed; refer to Figure 4 for an enlarged view of the core-pulling mechanism; refer to Figure 7 is a schematic diagram of the moving direction of the outer slider, the inner slider and the slider locking block in the core-pulling mechanism during demolding 8 is a front view of the mold for processing the router shell based on the inner and outer slider core-pulling mechanism provided by the embodiment of the application when it is demolded.
本申请实施例提供一种基于内外滑块抽芯机构加工路由器外壳的模具,包括:外滑块1、内滑块2、滑块锁紧块3、动模4和定模5。The embodiment of the present application provides a mold for processing a router casing based on an inner and outer slider core-pulling mechanism, including: an
所述外滑块1与所述定模5侧面活动连接,所述内滑块2与所述动模4侧面活动连接,所述定模5上设置有定模背板51,所述滑块锁紧块3固定在所述定模背板5上,所述外滑块1、内滑块2和滑块锁紧块3位于同一侧。The
所述滑块锁紧块3包括第一弯折部31和第二弯折部32,合模时,所述第一弯折部31插入所述外滑块1,所述第一弯折部31与所述外滑块1接触,所述第二弯折部32插入所述内滑块2,所述第二弯折部32与所述内滑块2接触。The
所述第一弯折部31和第二弯折部32一体成型,所述第一弯折部31和第二弯折部32之间夹角为钝角,所述第一弯折部31和第二弯折部32连接处向远离所述动模4方向弯折,以使脱模时,所述外滑块1朝远离所述定模5的方向移动,所述内滑块2朝靠近所述动模4的方向移动。The
在本申请实施例中由于所述第一弯折部31和第二弯折部32一体成型,所述第一弯折部31和第二弯折部32之间夹角为钝角,所述第一弯折部31和第二弯折部32连接处向远离所述动模4方向弯折,因此在所述滑块锁紧块3被所述定模背板51带动离开所述动模4时,所述滑块锁紧块3的第一弯折部31会给所述外滑块1一个水平向外的力(远离所述定模5的方向的力),而第二弯折部32会给所述内滑块2一个水平向内的力(朝靠近所述动模4的方向的力),在这两个水平力的作用下,不仅可以完成散热孔和接线孔的成型,也同时解除了散热孔和接线孔处的抱紧力,可以使整个路由器外壳顺利脱模。In the embodiment of the present application, since the first bending
需要说明的是本申请实施例加工的路由器外壳为市面上常见的路由器外壳,但是其接线孔与散热孔必须在路由器外壳的一侧。路由器接线孔以及路由器散热孔的大小可根据实际需要选择,可加工的路由器的外壳型号有:V2、BELL或PATHOS。It should be noted that the router casing processed in the embodiment of the present application is a common router casing on the market, but the wiring holes and the heat dissipation holes must be on one side of the router casing. The size of the router wiring holes and the router cooling holes can be selected according to the actual needs. The shell models of the routers that can be processed are: V2, BELL or PATHOS.
参见图5,为外滑块结构示意图。Referring to FIG. 5 , it is a schematic diagram of the structure of the outer slider.
进一步的,所述外滑块1包括:外滑块本体11、斜销孔12和外孔抽芯13,所述斜销孔12和外孔抽芯13设置在所述外滑块本体11上,所述斜销孔12的朝向与第一弯折部31的朝向一致,合模时,所述滑块锁紧块3插入所述斜销孔12。所述外孔抽芯13形状为棱柱或圆柱体,所述外孔抽芯13用于成型路由器外壳上的接线孔。Further, the
所述斜销孔12的朝向与所述第一弯折部31的朝向一致,便于第一弯折部31插入所述斜销孔12。所述外孔抽芯13的形状可根据实际接线孔的需求进行选择,优选的为棱柱。The orientation of the
参见图6,为内滑块结构示意图。Referring to FIG. 6 , it is a schematic diagram of the structure of the inner slider.
进一步的,所述内滑块2包括:内滑块本体21、斜销拉槽22和内孔抽芯23,所述斜销拉槽22和内孔抽芯23设置在所述内滑块本体21上,所述斜销拉槽22的朝向与第二弯折部32朝向一致,合模时,所述滑块锁紧块3插入所述斜销拉槽22。Further, the
所述内孔抽芯23为多个片状凸起,所述内孔抽芯23用于成型路由器外壳上的散热孔。所述内孔抽芯23为了成型散热孔,所述斜销拉槽22的朝向与所述第二弯折部32的朝向一致,以便于所述所述第二弯折部32的插入或拔出。所述内孔抽芯23的形状可根据实际生产中,散热孔的形状进行选择,优选的为多个片状。The inner hole core pulling 23 is a plurality of sheet-like protrusions, and the inner hole core pulling 23 is used to form the heat dissipation holes on the router shell. In order to form a heat dissipation hole in the inner hole core pulling 23, the direction of the oblique
进一步的,所述外滑块1与所述定模5侧面通过压片6活动连接。所述内滑块2与所述动模4侧面通过压片6活动连接。所述压片6将外滑块1和内滑块2分别与定模5或动模4活动连接,可使所述外滑块1和所述内滑块2可在水平方向上移动,移动的距离略大于接线孔和散热孔的深度。Further, the outer sliding
进一步的,所述外滑块、内滑块、滑块锁紧块的材料为:冷作模具钢SKD11、NAK80或S136。这些材料纯净度高、耐磨性好、韧性好且耐高温能承受温度骤变不易断裂。Further, the material of the outer slider, the inner slider and the slider locking block is: cold work die steel SKD11, NAK80 or S136. These materials have high purity, good wear resistance, good toughness and high temperature resistance, which can withstand sudden changes in temperature and are not easy to break.
需要说明的是本申请实施例涉及的模具模仁制作的主要步骤包括:模具模仁设计(总装图,零件图,标准件,BOM),定制毛坯材料,NC粗加工,热处理,NC精加工,放电加工(EDM),慢走丝加工(Wire EDM)模具成型表面抛光处理,模仁修配,组装试模(成型参数的调试),塑胶原料的干燥处理,最后通过成型机取得合格的成型产品。以上制作步骤是本领域技术人员可以获知的常规制作方法。It should be noted that the main steps of making the mold core involved in the embodiments of the present application include: mold core design (general assembly drawing, parts drawing, standard parts, BOM), custom blank material, NC roughing, heat treatment, NC finishing, Electrical discharge machining (EDM), Wire EDM (Wire EDM), mold forming surface polishing, mold core repair, mold assembly test (adjustment of molding parameters), drying of plastic raw materials, and finally obtain qualified molding products through the molding machine. The above fabrication steps are conventional fabrication methods known to those skilled in the art.
由以上技术方案可知,本申请提供一种基于内外滑块抽芯机构加工路由器外壳的模具,包括:外滑块1、内滑块2、滑块锁紧块3、动模4和定模5;所述外滑块1与所述定模5侧面活动连接,所述内滑块2与所述动模4侧面活动连接,所述定模5上设置有定模背板51,所述滑块锁紧块3固定在所述定模背板5上,所述外滑块1、内滑块2和滑块锁紧块3位于同一侧;所述滑块锁紧块3包括第一弯折部31和第二弯折部32,合模时,所述第一弯折部31插入所述外滑块1,所述第一弯折部31与所述外滑块1接触,所述第二弯折部32插入所述内滑块2,所述第二弯折部32与所述内滑块2接触;所述第一弯折部31和第二弯折部32一体成型,所述第一弯折部31和第二弯折部32之间夹角为钝角,所述第一弯折部31和第二弯折部32连接处向远离所述动模4方向弯折,以使脱模时,所述外滑块1朝远离所述定模5的方向移动,所述内滑块2朝靠近所述动模4的方向移动。As can be seen from the above technical solutions, the present application provides a mold for processing a router casing based on an inner and outer slider core-pulling mechanism, including: an
参见图7为在脱模时,抽芯机构中外滑块、内滑块和滑块锁紧块的移动方向示意图。图中外滑块往外移动也即所述外滑块1朝远离所述定模5的方向移动,内滑块往内移动也即所述内滑块2朝靠近所述动模4的方向移动。7 is a schematic diagram of the moving direction of the outer slider, the inner slider and the slider locking block in the core pulling mechanism during demolding. In the figure, the outer slider moves outward, that is, the
在实际应用中,本申请提供的一种基于内外滑块抽芯机构加工路由器外壳的模具,使用时,合模时动模4与定模5紧贴,滑块锁紧块3的第一弯折部31插入外滑块1,第一弯折部31与外滑块1接触,滑块锁紧块3的第二弯折部32插入内滑块2,第二弯折部32与内滑块2接触;脱模时,动模4与定模5分开,定模5上的定模背板51带动滑块锁紧块3从外滑块1和内滑块2内拔出,外滑块1朝远离定模5的方向移动,内滑块2朝靠近所述动模4的方向移动,待散热孔和接线孔脱模后,再从模具中顶出整个路由器外壳,脱模完成。由于在脱模时,优先松开散热孔和接线孔处对应的内滑块2和外滑块1,导致加工的路由器外壳的散热孔和接线孔处的抱紧力减小,进而整个路由器外壳几乎无抱紧力,进而避免脱模时外壳会向模具一侧移动,划伤加工的路由器的外壳。In practical applications, the present application provides a mold for processing router casings based on an inner and outer slider core-pulling mechanism. When in use, the
以上结合具体实施方式和范例性实例对本申请进行了详细说明,不过这些说明并不能理解为对本申请的限制。本领域技术人员理解,在不偏离本申请精神和范围的情况下,可以对本申请技术方案及其实施方式进行多种等价替换、修饰或改进,这些均落入本申请的范围内。本申请的保护范围以所附权利要求为准。The present application has been described in detail above with reference to specific embodiments and exemplary examples, but these descriptions should not be construed as a limitation on the present application. Those skilled in the art understand that, without departing from the spirit and scope of the present application, various equivalent replacements, modifications or improvements can be made to the technical solutions of the present application and the embodiments thereof, which all fall within the scope of the present application. The scope of protection of the present application is determined by the appended claims.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210687218.3A CN114919140A (en) | 2022-06-16 | 2022-06-16 | Mould for machining router shell based on inner and outer sliding block core-pulling mechanism |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210687218.3A CN114919140A (en) | 2022-06-16 | 2022-06-16 | Mould for machining router shell based on inner and outer sliding block core-pulling mechanism |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN114919140A true CN114919140A (en) | 2022-08-19 |
Family
ID=82813830
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210687218.3A Pending CN114919140A (en) | 2022-06-16 | 2022-06-16 | Mould for machining router shell based on inner and outer sliding block core-pulling mechanism |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114919140A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115384002A (en) * | 2022-09-23 | 2022-11-25 | 东莞市纳百医疗科技有限公司 | Injection mold with core pulling structure |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101117015A (en) * | 2007-09-03 | 2008-02-06 | 黄山市汽车电器有限公司 | Bended wedge inside and outside knockout core injection mould |
| CN201721014U (en) * | 2009-07-17 | 2011-01-26 | 江苏长三角模具城发展有限公司 | Injection mold for simultaneously pulling cores |
| CN103538211A (en) * | 2013-09-17 | 2014-01-29 | 宁波天龙电子股份有限公司 | Mechanism capable of pulling core in two directions in once die opening |
| CN106738703A (en) * | 2017-03-15 | 2017-05-31 | 合兴集团有限公司 | The side core-pulling method of side core-pulling mechanism, injection mold and injection mold |
| CN108327186A (en) * | 2017-03-12 | 2018-07-27 | 福建胜亚模具有限公司 | A kind of multidirectional core pulling locking gang mould tool |
| CN217891748U (en) * | 2022-06-16 | 2022-11-25 | 苏州硕贝德通讯技术有限公司 | Die for machining router shell based on inner and outer sliding block core-pulling mechanism |
-
2022
- 2022-06-16 CN CN202210687218.3A patent/CN114919140A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101117015A (en) * | 2007-09-03 | 2008-02-06 | 黄山市汽车电器有限公司 | Bended wedge inside and outside knockout core injection mould |
| CN201721014U (en) * | 2009-07-17 | 2011-01-26 | 江苏长三角模具城发展有限公司 | Injection mold for simultaneously pulling cores |
| CN103538211A (en) * | 2013-09-17 | 2014-01-29 | 宁波天龙电子股份有限公司 | Mechanism capable of pulling core in two directions in once die opening |
| CN108327186A (en) * | 2017-03-12 | 2018-07-27 | 福建胜亚模具有限公司 | A kind of multidirectional core pulling locking gang mould tool |
| CN106738703A (en) * | 2017-03-15 | 2017-05-31 | 合兴集团有限公司 | The side core-pulling method of side core-pulling mechanism, injection mold and injection mold |
| CN217891748U (en) * | 2022-06-16 | 2022-11-25 | 苏州硕贝德通讯技术有限公司 | Die for machining router shell based on inner and outer sliding block core-pulling mechanism |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115384002A (en) * | 2022-09-23 | 2022-11-25 | 东莞市纳百医疗科技有限公司 | Injection mold with core pulling structure |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109133588A (en) | Glass processing die and glass processing method | |
| CN116118056A (en) | Composite material air inlet channel product forming tool based on memory core die | |
| CN217891748U (en) | Die for machining router shell based on inner and outer sliding block core-pulling mechanism | |
| CN110091479A (en) | A kind of back-off loose-core injection mould | |
| CN210966921U (en) | Die special for die casting of motor shell | |
| TWI600620B (en) | Molding structure for manufacturing a molded glass part | |
| JP3793500B2 (en) | Embossed carrier tape manufacturing method and embossed carrier tape manufacturing apparatus | |
| CN211137977U (en) | Adapter card holder, power failure identification device and injection mold | |
| CN209493479U (en) | A dual-mold structure for hot-bending glass | |
| CN209738149U (en) | Steel injection mold with inserts locate function | |
| CN219006818U (en) | Injection mold with internal thread preparation mold insert | |
| CN111823514B (en) | Injection mold structure | |
| CN222972688U (en) | Hair straightener motor support mould | |
| CN221793614U (en) | Injection mold for terminal embedded structural parts | |
| CN101602238A (en) | Mold core and its processing method | |
| CN219768993U (en) | An inner core-pulling structure of an injection mold | |
| CN120984850B (en) | Be applied to high-efficient drawing of patterns mould structure of radiator backplate | |
| CN219311851U (en) | Positioning mechanism for hardware injection molding and injection mold | |
| CN220362904U (en) | Shell mould demolding structure, injection mould equipment and injection molding machine | |
| CN221659841U (en) | A high-precision undercut circular hole demoulding mechanism | |
| CN221913081U (en) | Fan protection net mould | |
| CN221584399U (en) | A mold slide structure | |
| CN220314067U (en) | A mold with an inclined ejector structure | |
| CN221968923U (en) | A flexible thermoforming mold for quickly changing mold cavities | |
| CN216100198U (en) | Mold demolding structure of metal rubber-coated product with compact structure |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |