CN111715923A - An uncoiling shearing die suitable for various roll widths and material thicknesses - Google Patents
An uncoiling shearing die suitable for various roll widths and material thicknesses Download PDFInfo
- Publication number
- CN111715923A CN111715923A CN202010600555.5A CN202010600555A CN111715923A CN 111715923 A CN111715923 A CN 111715923A CN 202010600555 A CN202010600555 A CN 202010600555A CN 111715923 A CN111715923 A CN 111715923A
- Authority
- CN
- China
- Prior art keywords
- lower die
- shearing
- plate
- block
- roll width
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23D—PLANING; SLOTTING; SHEARING; BROACHING; SAWING; FILING; SCRAPING; LIKE OPERATIONS FOR WORKING METAL BY REMOVING MATERIAL, NOT OTHERWISE PROVIDED FOR
- B23D15/00—Shearing machines or shearing devices cutting by blades which move parallel to themselves
- B23D15/06—Sheet shears
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23D—PLANING; SLOTTING; SHEARING; BROACHING; SAWING; FILING; SCRAPING; LIKE OPERATIONS FOR WORKING METAL BY REMOVING MATERIAL, NOT OTHERWISE PROVIDED FOR
- B23D33/00—Accessories for shearing machines or shearing devices
- B23D33/02—Arrangements for holding, guiding, and/or feeding work during the operation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23D—PLANING; SLOTTING; SHEARING; BROACHING; SAWING; FILING; SCRAPING; LIKE OPERATIONS FOR WORKING METAL BY REMOVING MATERIAL, NOT OTHERWISE PROVIDED FOR
- B23D33/00—Accessories for shearing machines or shearing devices
- B23D33/10—Stops for positioning work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23D—PLANING; SLOTTING; SHEARING; BROACHING; SAWING; FILING; SCRAPING; LIKE OPERATIONS FOR WORKING METAL BY REMOVING MATERIAL, NOT OTHERWISE PROVIDED FOR
- B23D35/00—Tools for shearing machines or shearing devices; Holders or chucks for shearing tools
- B23D35/005—Adjusting the position of the cutting members
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Shearing Machines (AREA)
Abstract
本发明公开了一种适用于多种卷宽与料厚的开卷剪板模,包括下模座、卷宽挡料块安装板、卷宽挡料轮、送料辅助滚轮组、下模剪板刀块、下模剪板刀块间隙调节垫片和板料滑板;两个所述卷宽挡料块安装板通过移动机构安装在下模座的一端,每个所述卷宽挡料块安装板的两端均转动安装有卷宽挡料轮,所述送料辅助滚轮组设置有若干组且间隔设置在两个所述卷宽挡料块安装板之间,所述板料滑板安装在所述下模座的另一端且向下倾斜设置,所述下模剪板刀块和下模剪板刀块间隙调节垫片设置在所述送料辅助滚轮组与所述板料滑板之间。可以更好的提高生产效率,降低人工成本、消除操作员受伤风险、提升方板料品质质量,减少模具开发数量和生产换模时间。
The invention discloses an uncoiling shearing die suitable for various coil widths and material thicknesses, comprising a lower die base, a coil width blocking block mounting plate, a coil width blocking wheel, a feeding auxiliary roller set, and a lower die shearing knife block, the lower die shearing plate, the knife block gap adjustment gasket and the sheet material slide plate; the two roll width stopper mounting plates are installed at one end of the lower die base through a moving mechanism, and each of the roll width stopper mounting plates Both ends are rotatably installed with roll width stopper wheels, the feeding auxiliary roller group is provided with several groups and is arranged at intervals between the two roll width stopper block mounting plates, and the sheet material slide plate is installed on the lower part. The other end of the die base is inclined downward, and the lower die shearing plate cutter block and the lower die shearing plate cutter block gap adjusting gasket are arranged between the feeding auxiliary roller set and the sheet material sliding plate. It can better improve production efficiency, reduce labor costs, eliminate the risk of operator injury, improve the quality of square sheets, and reduce the number of mold development and production mold change time.
Description
技术领域technical field
本发明涉及剪板模技术领域,尤其涉及一种适用于多种卷宽与料厚的开卷剪板模。The invention relates to the technical field of shearing dies, in particular to an uncoiling shearing die suitable for various roll widths and material thicknesses.
背景技术Background technique
随着汽车行业的高速发展,各大主机厂和零部件厂对产品生产效率要求越来越快,产品质量要求越来越高,但给出的成本越来越低。为了应对高效率的生产和产品质量,只能在模具工装上做不断的创新,我们要做到与时俱进,才不致于跟不上汽车行业的发展。所以提高生产效率,降低人力成本,将传统人工生产改为自动化,用机器取代人力是势在必行。With the rapid development of the automobile industry, major OEMs and parts factories have higher and faster requirements for product production efficiency and higher product quality requirements, but the given costs are getting lower and lower. In order to cope with high-efficiency production and product quality, we can only make continuous innovations in mold tooling. We must keep pace with the times so as not to fail to keep up with the development of the automotive industry. Therefore, it is imperative to improve production efficiency, reduce labor costs, change traditional manual production to automation, and replace human labor with machines.
发明内容SUMMARY OF THE INVENTION
针对上述现有技术的不足,本专利申请所要解决的技术问题是:如何提供一种适用于多种卷宽与料厚的开卷剪板模,以消除传统方板料生产中,需要使用剪板机,耗费大量人力成本,剪板时操作员受伤风险系数高,并且每张板料剪出会出现质量问题,减少模具开发数量和生产换模时间,降低用剪板机方板剪板的材料损耗。In view of the above-mentioned deficiencies of the prior art, the technical problem to be solved by this patent application is: how to provide an uncoiling shearing die suitable for various coil widths and material thicknesses, so as to eliminate the need to use shearing plates in the production of traditional square sheet materials It consumes a lot of labor costs, and the operator has a high risk of injury when shearing the plate, and there will be quality problems when each sheet is cut out, reducing the number of mold development and production mold change time, and reducing the use of shearing machine. loss.
为了实现上述目的,本发明采用了如下技术方案:In order to achieve the above object, the present invention adopts the following technical solutions:
一种适用于多种卷宽与料厚的开卷剪板模,包括下模座、卷宽挡料块安装板、卷宽挡料轮、送料辅助滚轮组、下模剪板刀块、下模剪板刀块间隙调节垫片和板料滑板;所述卷宽挡料块安装板设置有两个,两个所述卷宽挡料块安装板通过移动机构安装在下模座的一端,每个所述卷宽挡料块安装板的两端均转动安装有卷宽挡料轮,所述送料辅助滚轮组设置有若干组且间隔设置在两个所述卷宽挡料块安装板之间,位于外侧的送料辅助滚轮组通过支架与卷宽挡料块安装板固定连接,所述板料滑板安装在所述下模座的另一端且向下倾斜设置,所述下模剪板刀块和下模剪板刀块间隙调节垫片设置在所述送料辅助滚轮组与所述板料滑板之间,所述下模剪板刀块靠近所述板料滑板设置,所述下模剪板刀块和下模剪板刀块间隙调节垫片并列设置。An uncoiling shearing die suitable for various coil widths and material thicknesses, including a lower die base, a coil width stopper mounting plate, a coil width stopper wheel, a feeding auxiliary roller set, a lower die shearing plate knife block, a lower die Shearing plate and knife block gap adjustment gasket and sheet material sliding plate; two roll width stopper mounting plates are provided, and the two roll width stopper mounting plates are installed at one end of the lower die base through a moving mechanism, each Both ends of the roll width stopper mounting plate are rotatably installed with roll width stopper wheels, and the feeding auxiliary roller group is provided with several groups and is arranged between the two roll width stopper mounting plates at intervals, The feeding auxiliary roller group located on the outside is fixedly connected with the installation plate of the roll width stopper through the bracket, the sheet material sliding plate is installed on the other end of the lower die base and is inclined downward, and the lower die shearing plate cutter block and The lower die shearing plate blade block gap adjustment gasket is arranged between the feeding auxiliary roller set and the sheet material sliding plate, the lower die shearing plate blade block is arranged close to the sheet material sliding plate, and the lower die shearing plate blade Block and lower die shearing plate and knife block gap adjustment gasket are arranged side by side.
这样,在需要对卷料进行剪板时,卷料的一端放置在卷料架上,卷料的端部通过送料辅助滚轮组支撑,通过移动机构调整两个卷宽挡料块安装板之间的距离,利用卷宽挡料轮对卷料的侧边进行挡料以及限位,卷料的端部随着送料辅助滚轮组运动至需要切割的位置,上模板带动上模剪板刀块向下运动,利用上模剪板刀块与下模剪板刀块对卷料的需要切割的位置进行剪板,剪板之后的方料通过板料滑板滑下,完成下料。下模剪板刀块间隙调节垫片在使用时,根据卷料的料厚,查看料厚剪切所需的上模剪板刀块和下模剪板刀块之间的间隙值,然后调整下模剪板刀块间隙调节垫片的厚度,垫片上有具体的垫片厚度值标注,以此达到生产此种卷料料厚所需的剪切刀口间隙值。In this way, when the coil needs to be sheared, one end of the coil is placed on the coil rack, the end of the coil is supported by the feeding auxiliary roller group, and the distance between the two coil width stopper mounting plates is adjusted by the moving mechanism. The side of the coil is blocked and limited by the coil width stopper wheel. The end of the coil material moves to the position where it needs to be cut with the feeding auxiliary roller set, and the upper template drives the upper die shearing plate knife block to the cutting position. Down movement, use the upper die shearing block and the lower die shearing block to cut the position of the coil material to be cut, and the square material after the cutting board slides down through the sheet material slide plate to complete the blanking. When the lower die shearing plate knife block gap adjustment gasket is in use, according to the material thickness of the coil, check the gap value between the upper die shearing plate knife block and the lower die shearing plate knife block required for material thickness shearing, and then adjust The thickness of the gasket is adjusted by the gap between the lower die shearing plate and the blade, and the gasket is marked with the specific gasket thickness value, so as to achieve the shearing knife edge gap value required for the production of this type of coil material thickness.
进一步的,所述移动机构包括螺杆支座、螺杆和卷宽调节手摇柄,所述螺杆支座设置有两个且固定安装在所述下模座上,所述螺杆两端通过轴承安装在所述螺杆支座上,所述螺杆一端与所述卷宽调节手摇柄固定连接,所述螺杆上的螺纹旋向沿中间向两端的旋向相反,所述螺杆的两端均旋接配合有螺母,所述螺母向上固定安装有连接块,所述连接块与所述卷宽挡料块安装板的下表面固定连接。Further, the moving mechanism includes a screw support, a screw and a roll width adjustment hand crank, the screw support is provided with two and is fixedly installed on the lower die seat, and the two ends of the screw are installed on the lower die seat through bearings. On the screw support, one end of the screw is fixedly connected with the roll width adjustment hand crank, the screw thread on the screw is in opposite directions along the middle to the two ends, and both ends of the screw are screwed together. There is a nut, and a connection block is fixedly installed upward on the nut, and the connection block is fixedly connected with the lower surface of the installation plate of the roll width stopper block.
这样,通过转动卷宽调节手摇柄带动螺杆转动,螺杆通过螺母和连接块带动两个卷宽挡料块安装板相互靠近或远离,以根据不同的卷料宽度进行调整。In this way, the screw is rotated by rotating the roll width adjusting handle, and the screw drives the two roll width stopper mounting plates to approach or move away from each other through the nut and the connecting block, so as to be adjusted according to different roll widths.
进一步的,还包括导向机构,所述导向机构包括导向支架,所述导向支架上固定安装有导向杆,所述导向杆长度方向与所述螺杆长度方向相同,所述导向杆设置有2根且分别设置在所述螺杆的两侧,所述导向杆上滑动配合有导向块,所述导向块与所述卷宽挡料块安装板的下表面固定连接。Further, it also includes a guide mechanism, the guide mechanism includes a guide bracket, a guide rod is fixedly installed on the guide bracket, the length direction of the guide rod is the same as the length direction of the screw rod, and the guide rod is provided with two and They are respectively arranged on both sides of the screw rod, and a guide block is slidably fitted on the guide rod, and the guide block is fixedly connected with the lower surface of the roll width blocking block mounting plate.
这样,设置有导向杆和导向块,可以更好的对卷宽挡料块安装板的运动进行导向。In this way, a guide rod and a guide block are provided, which can better guide the movement of the installation plate of the roll width stopper block.
进一步的,所述送料辅助滚轮组包括滚轮安装架,所述滚轮安装架上转动安装有送料滚轮,所述滚轮安装架通过支座固定安装在所述下模座上,所述滚轮安装架设置在所述移动机构上方。Further, the feeding auxiliary roller set includes a roller mounting frame, on which a feeding roller is rotatably mounted, the roller mounting frame is fixedly installed on the lower die seat through a support, and the roller mounting frame is provided with above the moving mechanism.
这样,设置有送料滚轮,可以对卷料进行输送,减小摩擦力。In this way, a feeding roller is provided, which can transport the coil material and reduce the frictional force.
进一步的,所述送料辅助滚轮组与所述下模剪板刀块间隙调节垫片之间还设置有浮动式浮料架,所述浮动式浮料架通过浮动支架安装在所述下模座上,所述浮动式浮料架上安装有浮动滚轮,所述浮动滚轮的上端与所述送料滚轮的上端位于同一平面内。Further, a floating floating material frame is also arranged between the feeding auxiliary roller set and the lower die shearing plate knife block gap adjustment gasket, and the floating floating material frame is installed on the lower die base through a floating bracket. On the above, a floating roller is installed on the floating floating frame, and the upper end of the floating roller and the upper end of the feeding roller are located in the same plane.
这样,设置有浮动式浮料架,可以对剪切之前的卷料进行支撑,方便剪切。In this way, a floating floating material rack is provided, which can support the coil material before cutting, which is convenient for cutting.
进一步的,所述板料滑板上开设有滑槽,所述滑槽内通过转轴安装有下料滚轮,所述下料滚轮的外侧位于所述滑槽外。方便剪切后的方板下料。Further, a chute is provided on the sheet material slide plate, a feeding roller is installed in the chute through a rotating shaft, and the outer side of the feeding roller is located outside the chute. It is convenient for cutting the square plate after cutting.
综上,本适用于多种卷宽与料厚的开卷剪板模,可以更好的提高生产效率,降低人工成本、消除操作员受伤风险、提升方板料品质质量,减少模具开发数量和生产换模时间。In summary, this open-coil shearing die is suitable for a variety of coil widths and material thicknesses, which can better improve production efficiency, reduce labor costs, eliminate the risk of operator injury, improve the quality and quality of square sheets, and reduce the number of mold development and production. Die change time.
附图说明Description of drawings
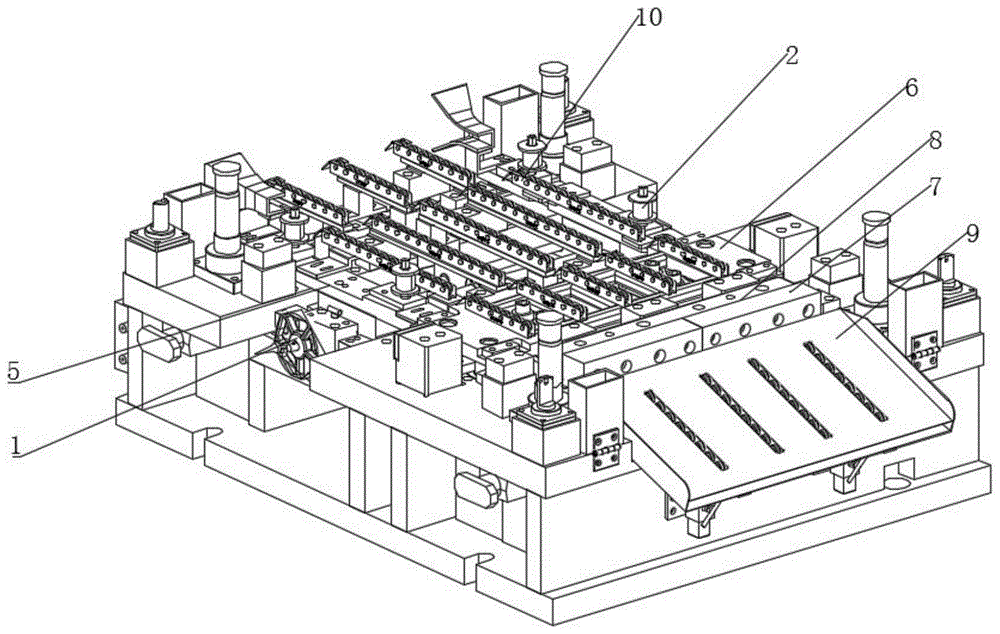
图1为本发明公开的适用于多种卷宽与料厚的开卷剪板模的结构示意图。FIG. 1 is a schematic structural diagram of an uncoiling shearing die suitable for various roll widths and material thicknesses disclosed in the present invention.
图2为图1的俯视图。FIG. 2 is a top view of FIG. 1 .
图3为图1的侧视图。FIG. 3 is a side view of FIG. 1 .
图4为上模板的仰视图。Figure 4 is a bottom view of the upper template.
具体实施方式Detailed ways
下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only a part of the embodiments of the present invention, but not all of the embodiments.
参照图1-4,一种适用于多种卷宽与料厚的开卷剪板模,包括下模座、卷宽挡料块安装板5、卷宽挡料轮2、送料辅助滚轮组10、下模剪板刀块7、下模剪板刀块间隙调节垫片8和板料滑板9;所述卷宽挡料块安装板5设置有两个,两个所述卷宽挡料块安装板5通过移动机构安装在下模座的一端,每个所述卷宽挡料块安装板5的两端均转动安装有卷宽挡料轮2,所述送料辅助滚轮组10设置有若干组且间隔设置在两个所述卷宽挡料块安装板5之间,位于外侧的送料辅助滚轮组10通过支架与卷宽挡料块安装板5固定连接,所述板料滑板9安装在所述下模座的另一端且向下倾斜设置,所述下模剪板刀块7和下模剪板刀块间隙调节垫片8设置在所述送料辅助滚轮组10与所述板料滑板9之间,所述下模剪板刀块7靠近所述板料滑板9设置,所述下模剪板刀块7和下模剪板刀块间隙调节垫片8并列设置。Referring to Figures 1-4, an uncoiling shearing die suitable for various roll widths and material thicknesses includes a lower die base, a roll width stopper
这样,在需要对卷料进行剪板时,卷料的一端放置在卷料架上,卷料的端部通过送料辅助滚轮组支撑,通过移动机构调整两个卷宽挡料块安装板之间的距离,利用卷宽挡料轮对卷料的侧边进行挡料以及限位,卷料的端部随着送料辅助滚轮组运动至需要切割的位置,上模板带动上模剪板刀块向下运动,利用上模剪板刀块与下模剪板刀块对卷料的需要切割的位置进行剪板,剪板之后的方料通过板料滑板滑下,完成下料。下模剪板刀块间隙调节垫片在使用时,根据卷料的料厚,查看料厚剪切所需的上模剪板刀块和下模剪板刀块之间的间隙值,然后调整下模剪板刀块间隙调节垫片的厚度,垫片上有具体的垫片厚度值标注,以此达到生产此种卷料料厚所需的剪切刀口间隙值。In this way, when the coil needs to be sheared, one end of the coil is placed on the coil rack, the end of the coil is supported by the feeding auxiliary roller group, and the distance between the two coil width stopper mounting plates is adjusted by the moving mechanism. The side of the coil is blocked and limited by the coil width stopper wheel. The end of the coil material moves to the position where it needs to be cut with the feeding auxiliary roller set, and the upper template drives the upper die shearing plate knife block to the cutting position. Down movement, use the upper die shearing block and the lower die shearing block to cut the position of the coil material to be cut, and the square material after the cutting board slides down through the sheet material slide plate to complete the blanking. When the lower die shearing plate knife block gap adjustment gasket is in use, according to the material thickness of the coil, check the gap value between the upper die shearing plate knife block and the lower die shearing plate knife block required for material thickness shearing, and then adjust The thickness of the gasket is adjusted by the gap between the lower die shearing plate and the blade, and the gasket is marked with the specific gasket thickness value, so as to achieve the shearing knife edge gap value required for the production of this type of coil material thickness.
本实施例中,所述移动机构包括螺杆支座、螺杆4和卷宽调节手摇柄1,所述螺杆支座设置有两个且固定安装在所述下模座上,所述螺杆4两端通过轴承安装在所述螺杆支座上,所述螺杆4一端与所述卷宽调节手摇柄1固定连接,所述螺杆4上的螺纹旋向沿中间向两端的旋向相反,所述螺杆4的两端均旋接配合有螺母,所述螺母向上固定安装有连接块,所述连接块与所述卷宽挡料块安装板5的下表面固定连接。In this embodiment, the moving mechanism includes a screw support, a screw 4 and a roll width adjusting
这样,通过转动卷宽调节手摇柄带动螺杆转动,螺杆通过螺母和连接块带动两个卷宽挡料块安装板相互靠近或远离,以根据不同的卷料宽度进行调整。In this way, the screw is rotated by rotating the roll width adjusting handle, and the screw drives the two roll width stopper mounting plates to approach or move away from each other through the nut and the connecting block, so as to be adjusted according to different roll widths.
本实施例中,还包括导向机构,所述导向机构包括导向支架,所述导向支架上固定安装有导向杆3,所述导向杆3长度方向与所述螺杆4长度方向相同,所述导向杆3设置有2根且分别设置在所述螺杆4的两侧,所述导向杆3上滑动配合有导向块,所述导向块与所述卷宽挡料块安装板5的下表面固定连接。In this embodiment, a guide mechanism is also included. The guide mechanism includes a guide bracket on which a guide rod 3 is fixedly installed. The length direction of the guide rod 3 is the same as the length direction of the screw 4. The guide rod 3 are provided with two and are respectively arranged on both sides of the screw 4 , the guide rod 3 is slidably fitted with a guide block, and the guide block is fixedly connected to the lower surface of the roll width stop
这样,设置有导向杆和导向块,可以更好的对卷宽挡料块安装板的运动进行导向。In this way, a guide rod and a guide block are provided, which can better guide the movement of the installation plate of the roll width stopper block.
本实施例中,所述送料辅助滚轮组10包括滚轮安装架,所述滚轮安装架上转动安装有送料滚轮,所述滚轮安装架通过支座固定安装在所述下模座上,所述滚轮安装架设置在所述移动机构上方。In this embodiment, the feeding
这样,设置有送料滚轮,可以对卷料进行输送,减小摩擦力。In this way, a feeding roller is provided, which can transport the coil material and reduce the frictional force.
本实施例中,所述送料辅助滚轮组10与所述下模剪板刀块间隙调节垫片8之间还设置有浮动式浮料架6,所述浮动式浮料架6通过浮动支架安装在所述下模座上,所述浮动式浮料架6上安装有浮动滚轮,所述浮动滚轮的上端与所述送料滚轮的上端位于同一平面内。In this embodiment, a floating
这样,设置有浮动式浮料架,可以对剪切之前的卷料进行支撑,方便剪切。In this way, a floating floating material rack is provided, which can support the coil material before cutting, which is convenient for cutting.
本实施例中,所述板料滑板9上开设有滑槽,所述滑槽内通过转轴安装有下料滚轮,所述下料滚轮的外侧位于所述滑槽外。方便剪切后的方板下料。In this embodiment, a chute is provided on the sheet slide 9, and a feed roller is installed in the chute through a rotating shaft, and the outer side of the feed roller is located outside the chute. It is convenient for cutting the square plate after cutting.
具体的,上模板上设置的上模剪板刀块12一侧还设置有上模压料机构11。上模的结构为现有结构,本专利申请中不再重复描述。Specifically, an upper
进一步的,further,
模具在生产前可通过人工摇动卷宽调节手摇柄将卷宽挡料块安装板调整到适合此次生产所需的卷宽位置,使卷宽导料轮达到控制卷料生产时不随意摆动和送料辅助滚轮组达到控制卷料送料方向平稳;Before the production of the mold, manually shake the roll width adjustment handle to adjust the roll width stopper mounting plate to the roll width position suitable for the production, so that the roll width guide wheel can not swing freely when controlling roll material production. And the feeding auxiliary roller group can control the feeding direction of the coil to be stable;
根据所生产的卷料料厚,查看料厚剪切所需剪板上、下刀块间隙值,调整下模剪板刀块间隙调节垫片(此垫片上刻有具体垫片厚度值),达到生产此种卷料料厚所需剪切刀口间隙值。According to the thickness of the coil material produced, check the gap value between the shearing plate and the lower knife block required for the shearing of the material thickness, and adjust the gap adjustment gasket of the lower die shearing plate and the knife block (the specific gasket thickness value is engraved on this gasket) , to achieve the cutting edge gap value required for the production of this kind of coil material thickness.
上模剪板刀块与上模固定,下模剪板刀块与下模固定,并在下模剪板刀块背面放置下模剪板刀块间隙调节垫片(此垫片上面刻有单张垫片的厚度值,分别为0.01mm,0.02mm,0.05mm调整垫片,并用螺钉锁附在下模剪板刀块靠背座上),另外分别准备20张0.01mm和0.02mm,10张0.05mm下模剪板刀块间隙调节垫片放于模具垫片储存盒内;初始模具剪板刀口间隙值设定为剪2.0mm料厚,在模具生产前根据所生产料厚,来调整剪板道口间隙值。The upper die shearing block is fixed with the upper die, the lower die shearing block is fixed with the lower die, and the lower die shearing block gap adjustment gasket is placed on the back of the lower die shearing block (this gasket is engraved with a leaflet The thickness of the shims are 0.01mm, 0.02mm, 0.05mm to adjust the shims, and they are locked on the back seat of the lower die shearing plate knife block with screws). In addition, prepare 20 sheets of 0.01mm and 0.02mm, and 10 sheets of 0.05mm. The lower die shearing plate blade gap adjustment gasket is placed in the die gasket storage box; the initial die shearing blade gap value is set to cut the material thickness of 2.0mm, and the shearing plate crossing is adjusted according to the thickness of the material produced before the mold is produced. gap value.
具体操作如下:1)当所生产料厚大于2.0mm料厚时,根据刀口间隙值变化,将下模剪板刀块背面的垫片取掉一部分以达到生产所需刀口间隙值;2)当所生产料厚小于2.0mm料厚时,根据刀口间隙值变化,在下模剪板刀块背面增加下模剪板刀块间隙调节垫片以达到生产所需刀口间隙值。The specific operations are as follows: 1) When the thickness of the produced material is greater than 2.0mm, according to the change of the knife edge gap value, remove a part of the gasket on the back of the knife block of the lower die shearing plate to achieve the required knife edge gap value for production; 2) When the production When the material thickness is less than 2.0mm, according to the change of the knife edge gap value, add a lower mold shear plate knife block gap adjustment gasket on the back of the lower die shearing plate knife block to achieve the required knife edge gap value for production.
原理:principle:
在需要对卷料进行剪板时,卷料的一端放置在卷料架上,卷料的端部通过送料辅助滚轮组支撑,通过移动机构调整两个卷宽挡料块安装板之间的距离,利用卷宽挡料轮对卷料的侧边进行挡料以及限位,卷料的端部随着送料辅助滚轮组运动至需要切割的位置,上模板带动上模剪板刀块向下运动,利用上模剪板刀块与下模剪板刀块对卷料的需要切割的位置进行剪板,剪板之后的方料通过板料滑板滑下,完成下料。下模剪板刀块间隙调节垫片在使用时,根据卷料的料厚,查看料厚剪切所需的上模剪板刀块和下模剪板刀块之间的间隙值,然后调整下模剪板刀块间隙调节垫片的厚度,垫片上有具体的垫片厚度值标注,以此达到生产此种卷料料厚所需的剪切刀口间隙值。When the coil needs to be sheared, one end of the coil is placed on the coil rack, the end of the coil is supported by the feeding auxiliary roller set, and the distance between the two coil width stopper mounting plates is adjusted by the moving mechanism , Use the roll width stop wheel to stop and limit the side of the roll material, the end of the roll material moves to the position that needs to be cut with the feeding auxiliary roller set, and the upper template drives the upper die shearing plate to move downward. , Use the upper die shearing block and the lower die shearing block to cut the position of the coil material to be cut, and the square material after the shearing board slides down through the plate slide plate to complete the blanking. When the lower die shearing plate knife block gap adjustment gasket is in use, according to the material thickness of the coil, check the gap value between the upper die shearing plate knife block and the lower die shearing plate knife block required for material thickness shearing, and then adjust The thickness of the gasket is adjusted by the gap between the lower die shearing plate and the blade, and the gasket is marked with the specific gasket thickness value, so as to achieve the shearing knife edge gap value required for the production of this type of coil material thickness.
以上所述,仅为本发明较佳的具体实施方式,但本发明的保护范围并不局限于此,任何熟悉本技术领域的技术人员在本发明揭露的技术范围内,根据本发明的技术方案及其发明构思加以等同替换或改变,都应涵盖在本发明的保护范围之内。The above description is only a preferred embodiment of the present invention, but the protection scope of the present invention is not limited to this. The equivalent replacement or change of the inventive concept thereof shall be included within the protection scope of the present invention.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010600555.5A CN111715923A (en) | 2020-06-28 | 2020-06-28 | An uncoiling shearing die suitable for various roll widths and material thicknesses |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010600555.5A CN111715923A (en) | 2020-06-28 | 2020-06-28 | An uncoiling shearing die suitable for various roll widths and material thicknesses |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111715923A true CN111715923A (en) | 2020-09-29 |
Family
ID=72569272
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010600555.5A Pending CN111715923A (en) | 2020-06-28 | 2020-06-28 | An uncoiling shearing die suitable for various roll widths and material thicknesses |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111715923A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112275891A (en) * | 2020-10-12 | 2021-01-29 | 湘潭地通汽车制品有限公司 | Blanking die with adjustable knife edge gap |
| CN112845801A (en) * | 2021-01-08 | 2021-05-28 | 奇瑞汽车河南有限公司 | Stamping sawtooth blanking die and using method thereof |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102847775A (en) * | 2012-08-21 | 2013-01-02 | 无锡美业机械制造有限公司 | Shearing plate die |
| CN103008443A (en) * | 2012-12-25 | 2013-04-03 | 仪征申威冲压有限公司 | Material sheet stamping device |
| CN207103647U (en) * | 2017-08-02 | 2018-03-16 | 安徽江淮汽车集团股份有限公司 | Rotate material supporting rack and uncoiling blanking mould |
| CN209716579U (en) * | 2019-01-19 | 2019-12-03 | 西安北方惠安防化设备有限公司 | A kind of plate shearing machine |
| CN210702799U (en) * | 2019-08-19 | 2020-06-09 | 贵州华夏电气有限公司 | Plate shearing device for production of low-voltage draw-out switch cabinet |
| CN212634471U (en) * | 2020-06-28 | 2021-03-02 | 重庆百能达普什汽车零部件有限责任公司 | Plate shearing die is cut in opening a book suitable for multiple width of rolling up with thick material |
-
2020
- 2020-06-28 CN CN202010600555.5A patent/CN111715923A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102847775A (en) * | 2012-08-21 | 2013-01-02 | 无锡美业机械制造有限公司 | Shearing plate die |
| CN103008443A (en) * | 2012-12-25 | 2013-04-03 | 仪征申威冲压有限公司 | Material sheet stamping device |
| CN207103647U (en) * | 2017-08-02 | 2018-03-16 | 安徽江淮汽车集团股份有限公司 | Rotate material supporting rack and uncoiling blanking mould |
| CN209716579U (en) * | 2019-01-19 | 2019-12-03 | 西安北方惠安防化设备有限公司 | A kind of plate shearing machine |
| CN210702799U (en) * | 2019-08-19 | 2020-06-09 | 贵州华夏电气有限公司 | Plate shearing device for production of low-voltage draw-out switch cabinet |
| CN212634471U (en) * | 2020-06-28 | 2021-03-02 | 重庆百能达普什汽车零部件有限责任公司 | Plate shearing die is cut in opening a book suitable for multiple width of rolling up with thick material |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112275891A (en) * | 2020-10-12 | 2021-01-29 | 湘潭地通汽车制品有限公司 | Blanking die with adjustable knife edge gap |
| CN112845801A (en) * | 2021-01-08 | 2021-05-28 | 奇瑞汽车河南有限公司 | Stamping sawtooth blanking die and using method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102990147A (en) | Belt cutting machine with pressure plate mechanism | |
| CN203156129U (en) | Belt cutting machine with platen mechanism | |
| CN206305251U (en) | a bending machine | |
| CN209716579U (en) | A kind of plate shearing machine | |
| CN102992082A (en) | Belt cutting machine with independently driven pressure plate mechanism | |
| CN219291527U (en) | Steel rolling waste recovery device | |
| CN209158937U (en) | A kind of laminator | |
| CN211638474U (en) | Cutting device of punching and cutting integrated machine | |
| CN210452888U (en) | Integrated art super-sensitive paper slitting device | |
| CN102990149B (en) | Belt cutting machine | |
| CN108465855B (en) | A multifunctional edge milling machine | |
| CN111185635B (en) | Battery pole piece high-speed slitting complete set of assembly line equipment | |
| CN209969779U (en) | A cutting device for mechanical engineering | |
| CN203343274U (en) | Aluminum honeycomb core rolling forming machine | |
| CN212634471U (en) | Plate shearing die is cut in opening a book suitable for multiple width of rolling up with thick material | |
| CN203156140U (en) | Belt cutting machine | |
| CN113954139B (en) | Straw building board shaping cutting machine | |
| CN203158900U (en) | Belt cutting machine with independent drive platen mechanism | |
| CN213971586U (en) | But spacing's cutting device | |
| CN115502460A (en) | Stepless adjustable blanking scissors for U-shaped steel formed part | |
| CN203156138U (en) | Belt cutting machine | |
| CN109807384A (en) | A kind of metal cutting machine | |
| CN203076687U (en) | Belt shearing machine | |
| CN207971237U (en) | Roller pricks molding machine | |
| CN209207655U (en) | The trimming device of guillotine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200929 |
|
| RJ01 | Rejection of invention patent application after publication |