CN111619216A - Corrugated board forming and printing integrated production line and use method - Google Patents
Corrugated board forming and printing integrated production line and use method Download PDFInfo
- Publication number
- CN111619216A CN111619216A CN202010588355.2A CN202010588355A CN111619216A CN 111619216 A CN111619216 A CN 111619216A CN 202010588355 A CN202010588355 A CN 202010588355A CN 111619216 A CN111619216 A CN 111619216A
- Authority
- CN
- China
- Prior art keywords
- roller
- printing
- ink
- paper guide
- production line
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 21
- 238000000034 method Methods 0.000 title claims description 8
- 239000011111 cardboard Substances 0.000 claims abstract description 30
- 239000000123 paper Substances 0.000 claims abstract description 28
- 238000007774 anilox coating Methods 0.000 claims abstract description 24
- 238000004049 embossing Methods 0.000 claims abstract description 21
- 238000009826 distribution Methods 0.000 claims abstract description 8
- 238000003854 Surface Print Methods 0.000 claims abstract description 7
- 239000000976 ink Substances 0.000 claims 19
- 238000007493 shaping process Methods 0.000 claims 1
- 238000005520 cutting process Methods 0.000 abstract description 11
- 239000002699 waste material Substances 0.000 abstract description 5
- 239000000463 material Substances 0.000 abstract description 3
- 238000011010 flushing procedure Methods 0.000 abstract 1
- 238000003892 spreading Methods 0.000 description 3
- 230000007812 deficiency Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 239000003638 chemical reducing agent Substances 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F19/00—Apparatus or machines for carrying out printing operations combined with other operations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F1/00—Mechanical deformation without removing material, e.g. in combination with laminating
- B31F1/20—Corrugating; Corrugating combined with laminating to other layers
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Rotary Presses (AREA)
Abstract
本发明公开的瓦楞纸板成型印刷一体生产线,包括双面机和设置在双面机后侧的底面印刷机;所述底面印刷机包括并列设置的若干个机组,所述机组中可转动的设置有压印辊、印刷辊、网纹辊、匀墨胶辊和导纸辊,所述印刷辊、网纹辊与匀墨胶辊水平并列设置,所述压印辊配合设置在印刷辊的正上侧,所述网纹辊与匀墨胶辊的下侧设置有接墨槽,所述导纸辊设置在机组的前侧,导纸辊之间的间隙与压印辊和印刷辊中间的间隙水平齐平本发明在双面机后侧直接对接底面印刷机,可直接对成型后的瓦楞纸板进行印刷工作,省去了裁切翻转纸板的步骤,提高生产效率,也避免了裁切产生费料的浪费,节省成本。
The corrugated cardboard forming and printing integrated production line disclosed by the invention comprises a duplexer and a bottom printing press arranged on the rear side of the duplexing machine; the bottom printing machine comprises several units arranged in parallel, and a rotatable unit is provided with Embossing roller, printing roller, anilox roller, ink-distributing rubber roller and paper guide roller, the printing roller, anilox roller and ink-distributing rubber roller are arranged horizontally side by side, and the embossing roller is arranged on the right side of the printing roller On the lower side of the anilox roller and the ink distribution rubber roller, there is an ink receiving groove, and the paper guide roller is arranged on the front side of the unit. The gap between the paper guide rollers and the gap between the embossing roller and the printing roller Horizontal flushing The invention is directly connected to the bottom surface printing machine on the back side of the double-sided machine, which can directly print the corrugated cardboard after forming, saves the step of cutting and turning the cardboard, improves the production efficiency, and also avoids the cost of cutting. waste of materials and cost savings.
Description
技术领域technical field
本发明涉及瓦楞纸生产设备技术领域,尤其涉及瓦楞纸板成型印刷一体生产线及使用方法。The invention relates to the technical field of corrugated cardboard production equipment, in particular to a corrugated cardboard forming and printing integrated production line and a use method.
背景技术Background technique
日常生活中应用广泛的纸箱均是由瓦楞纸板印刷模切后粘结而成的,可折叠成纸箱的瓦楞纸板包括如下制作步骤:双面机生产成型瓦楞纸板,然后印刷机对瓦楞纸板的面纸侧进行印刷,然后通入模切机进行模切,即完成对瓦楞纸板的加工,其中由双面机到印刷机的生产线中,双面机生产出的瓦楞纸板面纸在下侧,而印刷机则是上侧印刷,因此由双面机出来的瓦楞纸板需要裁切成大张,然后进行翻转,再通入印刷机进行印刷,操作麻烦,生产效率较低;并且这样加工出来的瓦楞纸板由于裁切尺寸的误差和预留量,不仅浪费水墨,还会在模切后产生许多费料,浪费大量成本。Cardboard boxes that are widely used in daily life are made of corrugated cardboard after printing and die-cutting. The corrugated cardboard that can be folded into a carton includes the following production steps: a double-sided machine produces a corrugated cardboard, and then the printing machine prints the surface of the corrugated cardboard. The paper side is printed, and then passed into the die-cutting machine for die-cutting, that is, the processing of the corrugated cardboard is completed. In the production line from the double-sided machine to the printing press, the corrugated cardboard surface paper produced by the double-sided machine is on the lower side, while the printing The machine is printed on the upper side, so the corrugated cardboard from the double-sided machine needs to be cut into large sheets, then turned over, and then passed into the printing machine for printing, which is troublesome to operate and has low production efficiency; and the corrugated cardboard processed in this way Due to the error of the cutting size and the reserved amount, not only the ink is wasted, but also a lot of waste materials after die-cutting, which wastes a lot of cost.
发明内容SUMMARY OF THE INVENTION
本发明的目的在于避免现有技术的不足之处,提供瓦楞纸板成型印刷一体生产线及使用方法,从而有效解决现有技术中存在的不足之处。The purpose of the present invention is to avoid the deficiencies of the prior art, and to provide a corrugated cardboard forming and printing integrated production line and a using method, thereby effectively solving the deficiencies in the prior art.
为实现上述目的,本发明采取的技术方案为:瓦楞纸板成型印刷一体生产线,包括双面机和设置在双面机后侧的底面印刷机;In order to achieve the above purpose, the technical scheme adopted in the present invention is: a corrugated cardboard forming and printing integrated production line, including a double-sided machine and a bottom surface printing machine arranged on the rear side of the double-sided machine;
所述底面印刷机包括并列设置的若干个机组,所述机组中可转动的设置有压印辊、印刷辊、网纹辊、匀墨胶辊和导纸辊,所述印刷辊、网纹辊与匀墨胶辊水平并列设置,所述压印辊配合设置在印刷辊的正上侧,所述网纹辊与匀墨胶辊的下侧设置有接墨槽,所述导纸辊设置在机组的前侧,导纸辊之间的间隙与压印辊和印刷辊中间的间隙水平齐平。The bottom surface printing machine includes several units arranged in parallel, and the unit is rotatably provided with an embossing roller, a printing roller, an anilox roller, an ink-distributing rubber roller and a paper guide roller. The printing roller, the anilox roller It is arranged horizontally and side by side with the ink distribution rubber roller, the embossing roller is arranged on the upper side of the printing roller, the anilox roller and the ink distribution rubber roller are provided with ink receiving grooves, and the paper guide roller is arranged on the lower side of the printing roller. On the front side of the unit, the gap between the paper guide rollers is level with the gap between the embossing roller and the printing roller.
进一步,所述压印辊的外端设置有齿轮套,压印辊通过轴承偏心设置在齿轮套上,所述机组上配合偏心齿轮套设置有调节齿轮。Further, the outer end of the embossing roller is provided with a gear sleeve, the embossing roller is eccentrically arranged on the gear sleeve through the bearing, and the unit is provided with an adjusting gear in cooperation with the eccentric gear sleeve.
进一步,所述接墨槽的下部设置有水墨箱,水墨箱上设置有水墨管,水墨管的上端由上到下指向网纹辊与匀墨胶辊之间,所述水墨管上设置有循环泵。Further, the lower part of the ink receiving tank is provided with an ink tank, the ink tank is provided with an ink pipe, the upper end of the ink pipe points from top to bottom between the anilox roller and the ink distribution rubber roller, and the ink pipe is provided with a circulation Pump.
进一步,所述机组之间设置有锁紧机构,所述锁紧机构包括铰接在机组后侧的气缸和卡板,卡板的另一端与气缸的活动端连接,机组的前侧配合相邻机组前侧的卡板设置有卡柱。Further, a locking mechanism is arranged between the units, and the locking mechanism includes a cylinder and a clamping plate hinged on the rear side of the unit, the other end of the clamping plate is connected with the movable end of the cylinder, and the front side of the unit cooperates with the adjacent unit. The card board on the front side is provided with a card post.
进一步,所述底面印刷机的前侧设置有与双面机连接的导纸平台,所述导纸平台包括方形的底座,底座上通过轮轴组设置有传送带,传送带的上表面与印刷辊的顶面齐平。Further, the front side of the bottom printing press is provided with a paper guide platform connected with the duplexer, the paper guide platform includes a square base, and a conveyor belt is arranged on the base through the wheel axle group, and the upper surface of the conveyor belt is connected to the top of the printing roller. face flush.
进一步,所述轮轴组包括端轮轴、定轮轴和撑紧轮轴,所述导纸平台的左右两端配合端轮轴均设置有驱动端轮轴左右移动的驱动装置,所述撑紧轮轴设置在定轮轴之间,撑紧轮轴通过支撑杆可上下移动的设置在底座上,所述底座上设置有趋向于迫使支撑杆顶住撑紧轮轴的弹簧。Further, the wheel shaft group includes an end wheel shaft, a fixed wheel shaft and a holding wheel shaft, the left and right ends of the paper guide platform are equipped with a driving device for driving the left and right movement of the end wheel shaft, and the holding wheel shaft is arranged on the fixed wheel shaft. In between, the tensioning wheel shaft is arranged on the base which can move up and down through the support rod, and the base is provided with a spring which tends to force the supporting rod against the tensioning wheel shaft.
瓦楞纸板成型印刷一体生产线的使用方法,包括如下过程:瓦楞纸板由双面机中成型送出,由两个导纸辊导向输送至压印辊与印刷辊之间,网纹辊与匀墨胶辊之间加有水墨,匀墨胶辊将水墨在网纹辊上摊开,网纹辊携带水墨均匀涂在印刷辊上,印刷辊与压印辊相对转动时对瓦楞纸板的底面直接进行印刷;The use method of the corrugated cardboard forming and printing integrated production line includes the following process: the corrugated cardboard is formed and sent out from the double-sided machine, guided and transported by two paper guide rollers to between the embossing roller and the printing roller, the anilox roller and the ink-spreading rubber roller Ink is added between them, and the ink-spreading rubber roller spreads the ink on the anilox roller, and the anilox roller carries the ink and evenly coats the printing roller. When the printing roller and the embossing roller rotate relative to each other, the bottom surface of the corrugated cardboard is directly printed;
网纹辊与匀墨胶辊上的水墨滴下时可滴在接墨槽中。The ink on the anilox roller and the ink-spreading rubber roller can be dropped in the ink tank when it is dropped.
本发明的上述技术方案具有以下有益效果:本发明在双面机后侧直接对接底面印刷机,可直接对成型后的瓦楞纸板进行印刷工作,省去了裁切翻转纸板的步骤,提高生产效率,也避免了裁切产生费料的浪费,节省成本。The above-mentioned technical scheme of the present invention has the following beneficial effects: the present invention directly connects to the bottom printing press on the back side of the double-sided machine, and can directly print the corrugated cardboard after forming, saves the step of cutting and turning the cardboard, and improves the production efficiency It also avoids the waste of cutting materials and saves costs.
附图说明Description of drawings
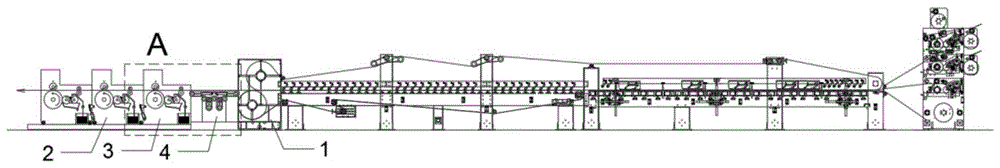
图1为本发明实施例的平面图;1 is a plan view of an embodiment of the present invention;
图2为图1中A处的放大图;Fig. 2 is the enlarged view of A place in Fig. 1;
图3为本发明实施例调节齿轮与齿轮套配合的示意图。FIG. 3 is a schematic diagram of the coordination between the adjusting gear and the gear sleeve according to the embodiment of the present invention.
具体实施方式Detailed ways
下面结合附图和实施例对本发明的实施方式作进一步详细描述。以下实施例用于说明本发明,但不能用来限制本发明的范围。The embodiments of the present invention will be described in further detail below with reference to the accompanying drawings and examples. The following examples are intended to illustrate the present invention, but not to limit the scope of the present invention.
在本发明的描述中,除非另有说明,“多个”的含义是两个或两个以上;术语“上”、“下”、“左”、“右”、“内”、“外”、“前端”、“后端”、“头部”、“尾部”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述本发明和简化描述,而不是指示或暗示所指的装置或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本发明的限制。在本发明的描述中,需要说明的是,除非另有明确的规定和限定,术语“相连”、“连接”应做广义理解,例如,可以是固定连接,也可以是可拆卸连接,或一体地连接;可以是机械连接,也可以是电连接;可以是直接相连,也可以通过中间媒介间接相连。对于本领域的普通技术人员而言,可以具体情况理解上述术语在本发明中的具体含义。In the description of the present invention, unless otherwise stated, "plurality" means two or more; the terms "upper", "lower", "left", "right", "inner", "outer" The orientation or positional relationship indicated by , "front end", "rear end", "head", "tail", etc. are based on the orientation or positional relationship shown in the accompanying drawings, and are only for the convenience of describing the present invention and simplifying the description, not An indication or implication that the referred device or element must have a particular orientation, be constructed and operate in a particular orientation, is not to be construed as a limitation of the invention. In the description of the present invention, it should be noted that, unless otherwise expressly specified and limited, the terms "connected" and "connected" should be understood in a broad sense, for example, it may be a fixed connection, a detachable connection, or an integral connection. Ground connection; it can be a mechanical connection or an electrical connection; it can be directly connected or indirectly connected through an intermediate medium. For those of ordinary skill in the art, the specific meanings of the above terms in the present invention can be understood in specific situations.
如图1-3所示,本实施例所述的瓦楞纸板成型印刷一体生产线,包括双面机1和设置在双面机1后侧的底面印刷机2;As shown in Figures 1-3, the corrugated cardboard forming and printing integrated production line described in this embodiment includes a double-
底面印刷机2包括并列设置的若干个机组3,机组3中可转动的设置有压印辊31、印刷辊32、网纹辊33、匀墨胶辊34和导纸辊35,印刷辊32、网纹辊33与匀墨胶辊34水平并列设置,压印辊31配合设置在印刷辊32的正上侧,网纹辊33与匀墨胶辊34的下侧设置有接墨槽36,导纸辊35设置在机组3的前侧,导纸辊35之间的间隙与压印辊31和印刷辊32中间的间隙水平齐平;The
瓦楞纸板由双面机1中成型送出,由两个导纸辊35导向输送至压印辊31与印刷辊32之间,网纹辊33与匀墨胶辊34之间加有水墨,匀墨胶辊34将水墨在网纹辊33上摊开,网纹辊33携带水墨均匀涂在印刷辊32上(网纹辊33与匀墨胶辊34上的水墨滴下时可滴在接墨槽36中),印刷辊32与压印辊31相对转动时对瓦楞纸板的底面直接进行印刷,省去了裁切翻转纸板的步骤,提高生产效率,也避免了裁切产生费料的浪费,节省成本。The corrugated cardboard is formed and sent out from the double-
优选的,压印辊31的外端设置有齿轮套311,压印辊31通过轴承313偏心设置在齿轮套311上,机组3上配合偏心齿轮套311设置有调节齿轮312,通过转动调节齿轮312可驱使齿轮套311转动,可对压印辊31的上下位置进行微调,从而调整压印辊31与印刷辊32之间的压力,其中调节齿轮312可通过减速机进行驱动转动。Preferably, the outer end of the
优选的,接墨槽36的下部设置有水墨箱361,水墨箱361上设置有水墨管362,水墨管362的上端由上到下指向网纹辊33与匀墨胶辊34之间,水墨管362上设置有循环泵;接墨槽36的下端设置有通向水墨箱361的开口,底面印刷机2工作时,水墨箱361中的水墨通过循环泵缓慢通入网纹辊33与匀墨胶辊34之间进行上墨。Preferably, an
优选的,机组3之间设置有锁紧机构21,锁紧机构21包括铰接在机组3后侧的气缸211和卡板212,卡板212的另一端与气缸211的活动端连接,机组3的前侧配合相邻机组3前侧的卡板212设置有卡柱213,机组3之间位置摆好之后,气缸211驱动卡板212转动,卡板212的前端勾住卡柱213,从而将机组3之间互相锁紧,避免机组3产生移动影响印刷准确性。Preferably, a
优选的,底面印刷机2的前侧设置有与双面机1连接的导纸平台4,导纸平台4包括方形的底座41,底座41上通过轮轴组设置有传送带42,传送带42的上表面与印刷辊32的顶面齐平,瓦楞纸板由双面机1送出后,可通过导纸平台4托住,输送至底面印刷机2处;导纸平台4的底座41为方形,底座41一侧贴合双面机1设置,另一侧贴合底面印刷机2设置,可方便底面印刷机2与双面机1之间进行对正。Preferably, the front side of the
优选的,轮轴组包括端轮轴43、定轮轴44和撑紧轮轴45,导纸平台4的左右两端配合端轮轴43均设置有驱动端轮轴43左右移动的驱动装置46,撑紧轮轴45设置在定轮轴44之间,撑紧轮轴45通过支撑杆47可上下移动的设置在底座41上,底座41上设置有趋向于迫使支撑杆47顶住撑紧轮轴45的弹簧;驱动装置46可驱动端轮轴43向外伸出,从而可近距离配合双面机1的出料口或底面印刷机2的进料口,端轮轴43左右移动时,弹簧可通过支撑杆47和撑紧轮轴45顶紧传送带42,提供传送带42的活动量;其中,驱动装置46可为气缸。Preferably, the wheel shaft group includes an
本发明的实施例是为了示例和描述起见而给出的,而并不是无遗漏的或者将本发明限于所公开的形式。很多修改和变化对于本领域的普通技术人员而言是显而易见的。选择和描述实施例是为了更好说明本发明的原理和实际应用,并且使本领域的普通技术人员能够理解本发明从而设计适于特定用途的带有各种修改的各种实施例。The embodiments of the present invention are presented for purposes of illustration and description, and are not intended to be exhaustive or to limit the invention to the form disclosed. Many modifications and variations will be apparent to those of ordinary skill in the art. The embodiment was chosen and described in order to better explain the principles of the invention and the practical application, and to enable others of ordinary skill in the art to understand the invention for various embodiments with various modifications as are suited to the particular use.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010588355.2A CN111619216A (en) | 2020-06-24 | 2020-06-24 | Corrugated board forming and printing integrated production line and use method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010588355.2A CN111619216A (en) | 2020-06-24 | 2020-06-24 | Corrugated board forming and printing integrated production line and use method |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111619216A true CN111619216A (en) | 2020-09-04 |
Family
ID=72268347
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010588355.2A Pending CN111619216A (en) | 2020-06-24 | 2020-06-24 | Corrugated board forming and printing integrated production line and use method |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111619216A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115610018A (en) * | 2022-12-19 | 2023-01-17 | 烟台新森新材料有限公司 | Tailoring and trimming equipment for manufacturing paper boxes |
| CN118372546A (en) * | 2024-05-10 | 2024-07-23 | 宣城市博思特日用品有限公司 | Intelligent printing equipment and method for printing on cup surface and paper cup processing technology |
Citations (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4587898A (en) * | 1977-10-12 | 1986-05-13 | Vepa Zellstoff - Und Papierholding Ag | Corrugated paper installation for manufacturing of printed corrugating paper cuts with a corrugated paper machine and a rotary printing machine integrated therein |
| US5671676A (en) * | 1995-04-27 | 1997-09-30 | Mitsubishi Jukogyo Kabushiki Kaisha | Flexographic printer |
| JP2000280447A (en) * | 1999-04-02 | 2000-10-10 | Rengo Co Ltd | Ink supply device for printing press |
| KR200248530Y1 (en) * | 2001-06-30 | 2001-10-31 | 주식회사 무꾸미 | Mat for cleaning an anilox roller in a printing machine |
| US20030183101A1 (en) * | 2002-04-01 | 2003-10-02 | Michael Owen | Printing ink pumping system |
| CN2608277Y (en) * | 2003-02-03 | 2004-03-31 | 刘羽 | Corrugated paper board vein surface printing mechanism |
| CN2848563Y (en) * | 2005-12-19 | 2006-12-20 | 湖北京山轻工机械股份有限公司 | Fixed down printing type printing machine |
| CN101058244A (en) * | 2006-04-20 | 2007-10-24 | 株式会社矶轮 | Method for printing corrugated cardboard sheets |
| CN201471825U (en) * | 2009-07-23 | 2010-05-19 | 深圳市网印巨星机电设备有限公司 | Automatic discharge device of automatic screen printing machine |
| CN203032060U (en) * | 2013-01-16 | 2013-07-03 | 高文举 | Lithographic plate offset press capable of directly printing multilayer corrugated boards |
| CN103987524A (en) * | 2011-10-24 | 2014-08-13 | 鲍勃斯脱梅克斯股份有限公司 | Adjustment method and device for printing machine |
| US20170087878A1 (en) * | 2015-09-24 | 2017-03-30 | Bhs Corrugated Maschinen-Und Anlagenbau Gmbh | Corrugated-board machine |
| US20170087900A1 (en) * | 2015-09-24 | 2017-03-30 | Bhs Corrugated Maschinen-Und Anlagenbau Gmbh | Corrugated-board machine |
| CN106553388A (en) * | 2015-09-24 | 2017-04-05 | Bhs波纹机械和设备制造有限公司 | corrugated cardboard manufacturing machine |
| CN107187191A (en) * | 2017-07-03 | 2017-09-22 | 东莞市科隆威自动化设备有限公司 | A kind of silicon slice printer |
| CN207433011U (en) * | 2017-10-11 | 2018-06-01 | 上海今昌纸箱机械制造有限公司 | Full-automatic double-face printing and die-cutting unit |
| CN207607218U (en) * | 2017-12-11 | 2018-07-13 | 佛山市三水三丰包装材料有限公司 | Unit is cleared up at a kind of corrugated board printing, corner cut, useless angle |
| CN208052794U (en) * | 2018-03-23 | 2018-11-06 | 合肥丹盛包装有限公司 | A kind of aqueous letterpress of corrugated board with environmental protection and energy saving function |
| CN212372947U (en) * | 2020-06-24 | 2021-01-19 | 河北林成包装机械制造有限公司 | Corrugated board forming and printing integrated production line |
-
2020
- 2020-06-24 CN CN202010588355.2A patent/CN111619216A/en active Pending
Patent Citations (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4587898A (en) * | 1977-10-12 | 1986-05-13 | Vepa Zellstoff - Und Papierholding Ag | Corrugated paper installation for manufacturing of printed corrugating paper cuts with a corrugated paper machine and a rotary printing machine integrated therein |
| US5671676A (en) * | 1995-04-27 | 1997-09-30 | Mitsubishi Jukogyo Kabushiki Kaisha | Flexographic printer |
| JP2000280447A (en) * | 1999-04-02 | 2000-10-10 | Rengo Co Ltd | Ink supply device for printing press |
| KR200248530Y1 (en) * | 2001-06-30 | 2001-10-31 | 주식회사 무꾸미 | Mat for cleaning an anilox roller in a printing machine |
| US20030183101A1 (en) * | 2002-04-01 | 2003-10-02 | Michael Owen | Printing ink pumping system |
| CN2608277Y (en) * | 2003-02-03 | 2004-03-31 | 刘羽 | Corrugated paper board vein surface printing mechanism |
| CN2848563Y (en) * | 2005-12-19 | 2006-12-20 | 湖北京山轻工机械股份有限公司 | Fixed down printing type printing machine |
| CN101058244A (en) * | 2006-04-20 | 2007-10-24 | 株式会社矶轮 | Method for printing corrugated cardboard sheets |
| CN201471825U (en) * | 2009-07-23 | 2010-05-19 | 深圳市网印巨星机电设备有限公司 | Automatic discharge device of automatic screen printing machine |
| CN103987524A (en) * | 2011-10-24 | 2014-08-13 | 鲍勃斯脱梅克斯股份有限公司 | Adjustment method and device for printing machine |
| CN203032060U (en) * | 2013-01-16 | 2013-07-03 | 高文举 | Lithographic plate offset press capable of directly printing multilayer corrugated boards |
| US20170087878A1 (en) * | 2015-09-24 | 2017-03-30 | Bhs Corrugated Maschinen-Und Anlagenbau Gmbh | Corrugated-board machine |
| US20170087900A1 (en) * | 2015-09-24 | 2017-03-30 | Bhs Corrugated Maschinen-Und Anlagenbau Gmbh | Corrugated-board machine |
| CN106553388A (en) * | 2015-09-24 | 2017-04-05 | Bhs波纹机械和设备制造有限公司 | corrugated cardboard manufacturing machine |
| CN107187191A (en) * | 2017-07-03 | 2017-09-22 | 东莞市科隆威自动化设备有限公司 | A kind of silicon slice printer |
| CN207433011U (en) * | 2017-10-11 | 2018-06-01 | 上海今昌纸箱机械制造有限公司 | Full-automatic double-face printing and die-cutting unit |
| CN207607218U (en) * | 2017-12-11 | 2018-07-13 | 佛山市三水三丰包装材料有限公司 | Unit is cleared up at a kind of corrugated board printing, corner cut, useless angle |
| CN208052794U (en) * | 2018-03-23 | 2018-11-06 | 合肥丹盛包装有限公司 | A kind of aqueous letterpress of corrugated board with environmental protection and energy saving function |
| CN212372947U (en) * | 2020-06-24 | 2021-01-19 | 河北林成包装机械制造有限公司 | Corrugated board forming and printing integrated production line |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115610018A (en) * | 2022-12-19 | 2023-01-17 | 烟台新森新材料有限公司 | Tailoring and trimming equipment for manufacturing paper boxes |
| CN118372546A (en) * | 2024-05-10 | 2024-07-23 | 宣城市博思特日用品有限公司 | Intelligent printing equipment and method for printing on cup surface and paper cup processing technology |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201437291U (en) | Pressure regulating device of intermittent rotary printing unit | |
| US5558021A (en) | Printing device for printing plastic cards | |
| CN208052794U (en) | A kind of aqueous letterpress of corrugated board with environmental protection and energy saving function | |
| CN212372947U (en) | Corrugated board forming and printing integrated production line | |
| CN210680015U (en) | Relief printing device | |
| CN217622722U (en) | An automatic plate changing device for a printing press | |
| CN220115763U (en) | A printing machine loading device | |
| CN208069090U (en) | A fixed-length high-efficiency cutting device for offset printing machines for color card production | |
| CN214239939U (en) | Aluminum foil bag flexo printing feeding mechanism | |
| CN211641414U (en) | Flexo press two-sided printing transparent ink positioner | |
| CN213891697U (en) | Stereo picture and text printing device | |
| CN213294163U (en) | Printing paper loading attachment | |
| CN215970595U (en) | Automatic positioning device of intaglio printing machine suitable for plastic material printing | |
| CN223073553U (en) | Feeding device of printing machine | |
| CN220165287U (en) | Conveying mechanism of decorative paper intaglio printing press | |
| CN222293087U (en) | Unreeling device of rotary printing machine | |
| CN220866644U (en) | Embossing device | |
| CN214934346U (en) | A green energy-saving printing equipment | |
| CN218491006U (en) | Paper feeding mechanism for printing machine | |
| CN221318483U (en) | Paper pressing equipment of printing machine | |
| CN117841520B (en) | Printing device and method based on paper transfer function | |
| CN221893845U (en) | Cardboard conveying device | |
| CN220808871U (en) | Packaging printing machine with drying structure | |
| CN223340259U (en) | Printing device of a printing press | |
| CN222554502U (en) | A device for expanding flexographic printing roller into intermittent lamination |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200904 |
|
| RJ01 | Rejection of invention patent application after publication |