CN111342108A - A batch sealing device for button lithium battery - Google Patents
A batch sealing device for button lithium battery Download PDFInfo
- Publication number
- CN111342108A CN111342108A CN202010184362.6A CN202010184362A CN111342108A CN 111342108 A CN111342108 A CN 111342108A CN 202010184362 A CN202010184362 A CN 202010184362A CN 111342108 A CN111342108 A CN 111342108A
- Authority
- CN
- China
- Prior art keywords
- plate
- sealing
- sealing device
- punching
- forming die
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/04—Construction or manufacture in general
- H01M10/0404—Machines for assembling batteries
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/04—Construction or manufacture in general
- H01M10/0422—Cells or battery with cylindrical casing
- H01M10/0427—Button cells
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M6/00—Primary cells; Manufacture thereof
- H01M6/005—Devices for making primary cells
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/50—Manufacturing or production processes characterised by the final manufactured product
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Sealing Battery Cases Or Jackets (AREA)
Abstract
本发明公开了一种纽扣锂电池的批量封口装置,包括机架底板,所述机架底板的顶部固定连接有机架立板,所述机架立板的顶部设有机架上板,所述机架上板的顶部安装有液压缸,所述液压缸的输出轴上安装有冲针夹板,所述冲针夹板的底部设有冲针,所述冲针的外部设有脱料板,所述机架立板的内侧设有封口仓,所述定位板的顶部活动连接有周转盘,所述周转盘的顶部活动连接有推盘。在封口时,将钮电池排列在推盘中,然后将周转盘和推盘放到定位板上,开启液压缸带动冲针进行封口工作,液压下压,在封口装置对面人工取出,封口工序完成,因为人机结合,无论是封口模具,还是封口的稳定性都得到了极大的提高。

The invention discloses a batch sealing device for button lithium batteries. A hydraulic cylinder is installed on the top of the upper plate of the frame, a punching pin splint is installed on the output shaft of the hydraulic cylinder, a punching needle is arranged at the bottom of the punching needle splint, and a stripping plate is arranged on the outside of the punching needle, The inner side of the frame vertical plate is provided with a sealing bin, the top of the positioning plate is movably connected with an epicyclic disk, and the top of the epicyclic disk is movably connected with a push plate. When sealing, the button batteries are arranged in the push plate, then the turntable and push plate are placed on the positioning plate, the hydraulic cylinder is opened to drive the punching needle to perform the sealing work, the hydraulic pressure is pressed down, and it is manually removed from the opposite side of the sealing device, and the sealing process is completed. , Because of the combination of man and machine, both the sealing mold and the stability of the sealing have been greatly improved.
Description
技术领域technical field
本发明涉及纽扣电池生产技术领域,具体为一种纽扣锂电池的批量封口装置。The invention relates to the technical field of button battery production, in particular to a batch sealing device for button lithium batteries.
背景技术Background technique
纽扣电池的封口一般都是利用冲床或液压一粒一粒的单只封口,无形中对封口模具的使用寿命,将很大程度地缩短,封装过程中也较容易出现故障。对纽扣锂电池而言,由于其特殊性,所有的装配、封口过程必须在极度干燥、密闭的环境下作业,较大型号纽扣锂电池无论是冲床封口还是液压封口,相对都比较稳定,但小型号纽扣锂电池的封口,稳定性和效率任然是个问题。The sealing of button batteries is generally single-sealed by punching or hydraulic pressure. Invisibly, the service life of the sealing mold will be shortened to a large extent, and failures are more likely to occur during the packaging process. For button lithium batteries, due to their particularity, all assembly and sealing processes must be performed in an extremely dry and airtight environment. Larger type button lithium batteries are relatively stable, whether punch sealing or hydraulic sealing, but small. The sealing, stability and efficiency of the model button lithium battery are still a problem.
发明内容SUMMARY OF THE INVENTION
本发明的目的在于提供一种纽扣锂电池的批量封口装置,在封口时,将钮电池排列在推盘中,然后将周转盘和推盘放到定位板上,再把推盘及推盘内的待封口电池一起推入封口仓内,开启液压缸带动冲针进行封口工作,液压下压,完成封口动作,液压上升回位待命,重复待封口电池推入工序,第一盘已封口的电池及推盘被推出,在封口装置对面人工取出,封口工序完成,因为人机结合,无论是封口模具,还是封口的稳定性都得到了极大的提高。The purpose of the present invention is to provide a batch sealing device for button lithium batteries. When sealing, the button batteries are arranged in the push plate, and then the turntable and the push plate are placed on the positioning plate, and then the push plate and the push plate are placed in the push plate. The battery to be sealed is pushed into the sealing chamber together, the hydraulic cylinder is opened to drive the punching needle to perform the sealing work, the hydraulic pressure is pressed down to complete the sealing action, the hydraulic pressure is raised and returned to stand by, and the process of pushing the battery to be sealed is repeated. And the push plate is pushed out, and it is manually taken out on the opposite side of the sealing device, and the sealing process is completed. Because of the combination of man and machine, both the sealing mold and the sealing stability have been greatly improved.
为实现上述目的,本发明提供如下技术方案:一种纽扣锂电池的批量封口装置,包括机架底板,所述机架底板的顶部固定连接有机架立板,所述机架立板的顶部设有机架上板,所述机架上板的顶部安装有液压缸,所述液压缸的输出轴上安装有冲针夹板,所述冲针夹板的底部设有冲针,所述冲针的外部设有脱料板,所述机架立板的内侧设有封口仓,所述封口仓的内部安装有成型模夹板,所述成型模夹板的一端设有定位板,所述定位板的顶部活动连接有周转盘,所述周转盘的顶部活动连接有推盘;In order to achieve the above purpose, the present invention provides the following technical solutions: a batch sealing device for button lithium batteries, comprising a rack bottom plate, a rack vertical plate is fixedly connected to the top of the rack bottom plate, and the top of the rack vertical plate is There is an upper frame of the frame, a hydraulic cylinder is installed on the top of the upper frame of the frame, a punching pin splint is installed on the output shaft of the hydraulic cylinder, and a punching needle is arranged at the bottom of the punching needle clamping plate, and the punching needle is There is a stripping board on the outside of the frame, a sealing bin is provided on the inner side of the frame vertical plate, a forming die clamp is installed inside the sealing bin, and one end of the forming die splint is provided with a positioning plate. The top is movably connected with a turntable, and the top of the turntable is movably connected with a push plate;
所述成型模夹板的顶部两侧均焊接有与推盘相匹配的L型限位板,所述L型限位板的内侧开设有弹簧槽,所述弹簧槽的内部安装有第一弹簧,所述第一弹簧的端部设有钢珠,所述钢珠活动插接于球窝的内部,所述球窝开设于推盘的边部。Both sides of the top of the forming die clamp plate are welded with L-shaped limit plates matching the push plates, a spring groove is opened on the inner side of the L-shaped limit plate, and a first spring is installed inside the spring groove. The end of the first spring is provided with a steel ball, the steel ball is movably inserted into the inside of the ball socket, and the ball socket is opened on the edge of the push plate.
优选的,所述冲针夹板的内部开设有导向孔,所述导向孔的内部插接有导向杆,所述导向杆固定连接与机架底板和机架上板之间。Preferably, a guide hole is formed inside the punching clamp plate, and a guide rod is inserted into the inside of the guide hole, and the guide rod is fixedly connected with the bottom plate of the frame and the upper plate of the frame.
优选的,所述导向孔的内部插接有直线轴承,所述直线轴承套接于导向杆的外部。Preferably, a linear bearing is inserted into the inside of the guide hole, and the linear bearing is sleeved on the outside of the guide rod.
优选的,所述定位板的一端固定连接有限位柱,所述周转盘的底部开设有与限位柱相匹配的限位孔。Preferably, one end of the positioning plate is fixedly connected to a limit post, and a limit hole matching the limit post is opened at the bottom of the turntable.
优选的,所述冲针夹板的底部与脱料板的顶部之间固定连接有第二弹簧,且脱料板上开设有与冲针相匹配的通孔。Preferably, a second spring is fixedly connected between the bottom of the punching clamp plate and the top of the stripping plate, and the stripping plate is provided with a through hole matching the punching needle.
优选的,所述成型模夹板的另一端设有工作平台,所述工作平台的顶部与成型模夹板的顶部设在同一水平面上。Preferably, the other end of the forming die clamp is provided with a working platform, and the top of the working platform and the top of the forming die clamp are set on the same level.
与现有技术相比,本发明的有益效果是:Compared with the prior art, the beneficial effects of the present invention are:
1、本发明主要由机架底板、液压缸、成型模夹板、周转盘、推盘等部件构成,在封口时,将钮电池排列在推盘中,然后将周转盘和推盘放到定位板上,再把推盘及推盘内的待封口电池一起推入封口仓内,开启液压缸带动冲针进行封口工作,液压下压,完成封口动作,液压上升回位待命,重复待封口电池推入工序,第一盘已封口的电池及推盘被推出,在封口装置对面人工取出,封口工序完成,因为人机结合,无论是封口模具,还是封口的稳定性都得到了极大的提高;1. The present invention is mainly composed of a frame bottom plate, a hydraulic cylinder, a forming die splint, a turntable, a pusher, etc. When sealing, the button batteries are arranged in the pusher, and then the turntable and the pusher are placed on the positioning plate. Then push the push plate and the battery to be sealed in the push plate into the sealing chamber together, open the hydraulic cylinder to drive the punching needle to perform the sealing work, press down the hydraulic pressure to complete the sealing action, the hydraulic pressure rises and returns to standby, repeat the push of the battery to be sealed. After entering the process, the first sealed battery and push plate are pushed out, and manually taken out on the opposite side of the sealing device. The sealing process is completed. Because of the combination of man and machine, both the sealing mold and the sealing stability have been greatly improved;
2、本发明在成型模夹板的顶部两侧设置L型限位板,用来限制推盘在成型模夹板上的位置,在将推盘推入到成型模夹板上之后,弹簧槽中的弹簧挤压钢珠插在推盘边部的球窝中,有利于对推盘的定位,同时便于推盘的退出。2. In the present invention, L-shaped limit plates are arranged on both sides of the top of the forming die clamp plate to limit the position of the push plate on the forming die clamp plate. After the push plate is pushed into the forming die clamp plate, the spring in the spring groove The extruded steel ball is inserted into the ball socket on the edge of the push plate, which is beneficial to the positioning of the push plate and facilitates the withdrawal of the push plate.
附图说明Description of drawings
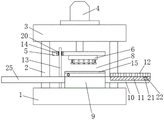
图1为本发明的结构示意图;Fig. 1 is the structural representation of the present invention;
图2为本发明推盘位于成型模夹板顶部时剖面结构示意图;Fig. 2 is the cross-sectional structure schematic diagram when the push plate of the present invention is positioned at the top of the forming die plate;
图3为本发明脱料板的剖面结构示意图;Fig. 3 is the sectional structure schematic diagram of the stripper plate of the present invention;
图4为本发明周转盘和推盘的结构示意图。FIG. 4 is a schematic structural diagram of the turntable and the pusher of the present invention.
图中:1、机架底板;2、机架立板;3、机架上板;4、液压缸;5、冲针夹板;6、冲针;7、脱料板;8、封口仓;9、成型模夹板;10、定位板;11、周转盘;12、推盘;13、导向杆;14、导向孔;15、L型限位板;16、弹簧槽;17、第一弹簧;18、钢珠;19、球窝;20、直线轴承;21、限位柱;22、限位孔;23、第二弹簧;24、通孔;25、工作平台。In the figure: 1. The bottom plate of the frame; 2. The vertical plate of the frame; 3. The upper plate of the frame; 4. The hydraulic cylinder; 5. The punching splint; 6. The punching; 9. Forming die clamping plate; 10. Positioning plate; 11. Turntable; 12. Push plate; 13. Guide rod; 14. Guide hole; 15. L-shaped limit plate; 16. Spring groove; 17. First spring; 18, steel ball; 19, ball socket; 20, linear bearing; 21, limit column; 22, limit hole; 23, second spring; 24, through hole; 25, working platform.
具体实施方式Detailed ways
下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only a part of the embodiments of the present invention, but not all of the embodiments. Based on the embodiments of the present invention, all other embodiments obtained by those of ordinary skill in the art without creative efforts shall fall within the protection scope of the present invention.
请参阅图1~4,本发明提供一种技术方案:一种纽扣锂电池的批量封口装置,包括机架底板1,机架底板1的顶部固定连接有机架立板2,机架立板2的顶部设有机架上板3,机架上板3的顶部安装有液压缸4,液压缸4的输出轴上安装有冲针夹板5,冲针夹板5的底部设有冲针6,冲针6的外部设有脱料板7,机架立板2的内侧设有封口仓8,封口仓8的内部安装有成型模夹板9,成型模夹板9的一端设有定位板10,定位板10的顶部活动连接有周转盘11,周转盘11的顶部活动连接有推盘12,推盘12上排列有与纽扣电池相匹配的孔,用来放置电池;1 to 4, the present invention provides a technical solution: a batch sealing device for button lithium batteries, comprising a
成型模夹板9的顶部两侧均焊接有与推盘12相匹配的L型限位板15,L型限位板15的内侧开设有弹簧槽16,弹簧槽16的内部安装有第一弹簧17,第一弹簧17的端部设有钢珠18,钢珠18活动插接于球窝19的内部,球窝19开设于推盘12的边部。Both sides of the top of the forming
在冲针夹板5的内部开设有导向孔14,导向孔14的内部插接有导向杆13,导向杆13固定连接与机架底板1和机架上板3之间,通过导向孔14和导向杆13的配合有利于限制住冲针夹板5的角度,提高冲针夹板5上下运行的直线性,在导向孔14的内部插接有直线轴承20,直线轴承20套接于导向杆13的外部,通过直线轴承20的设置,可以减少导向孔14和导向杆13的摩擦力。A guide hole 14 is opened inside the punching clamp plate 5, and a guide rod 13 is inserted into the guide hole 14. The guide rod 13 is fixedly connected with the
在定位板10的一端固定连接有限位柱21,周转盘11的底部开设有与限位柱21相匹配的限位孔22,通过限位柱21和限位孔22的配合,有利于限定周转盘11在定位板10上的位置,便于将推盘12推入到封口仓8中。在冲针夹板5的底部与脱料板7的顶部之间固定连接有第二弹簧23,且脱料板7上开设有与冲针6相匹配的通孔24,该通孔24便于脱料板7套在冲针6外部,第二弹簧23可以挤压脱料板7,防止冲针6将电池带起来,在成型模夹板9的另一端设有工作平台25,工作平台25的顶部与成型模夹板9的顶部设在同一水平面上,便于将封口后的推盘12推入到工作平台25上,进行取出电池。A
工作原理:在封口时,将钮电池排列在推盘12中,然后将周转盘11和推盘12放到定位板10上,再把推盘12及推盘12内的待封口电池一起推入封口仓8内,在将推盘12推入到成型模夹板9上之后,弹簧槽16中的第一弹簧17挤压钢珠18插在推盘12边部的球窝19中,有利于对推盘12的定位,开启液压缸4带动冲针6进行封口工作,液压缸4下压,完成封口动作,液压缸4上升回位待命,重复待封口电池推入工序,第一盘已封口的电池及推盘12被推出,在封口装置对面人工取出,封口工序完成,因为人机结合,无论是封口模具,还是封口的稳定性都得到了极大的提高。Working principle: when sealing, arrange the button batteries in the
尽管已经示出和描述了本发明的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本发明的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本发明的范围由所附权利要求及其等同物限定。Although embodiments of the present invention have been shown and described, it will be understood by those skilled in the art that various changes, modifications, and substitutions can be made in these embodiments without departing from the principle and spirit of the invention and modifications, the scope of the present invention is defined by the appended claims and their equivalents.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010184362.6A CN111342108B (en) | 2020-03-17 | 2020-03-17 | A batch sealing device for button lithium batteries |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010184362.6A CN111342108B (en) | 2020-03-17 | 2020-03-17 | A batch sealing device for button lithium batteries |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN111342108A true CN111342108A (en) | 2020-06-26 |
| CN111342108B CN111342108B (en) | 2025-03-07 |
Family
ID=71182454
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010184362.6A Active CN111342108B (en) | 2020-03-17 | 2020-03-17 | A batch sealing device for button lithium batteries |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111342108B (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111864163A (en) * | 2020-06-29 | 2020-10-30 | 江西新威动力能源科技有限公司 | Squeeze separator acid equipment with separator take-out mechanism |
| CN112259779A (en) * | 2020-10-21 | 2021-01-22 | 深圳市合壹新能技术有限公司 | Packaging machine |
| CN112382770A (en) * | 2021-01-13 | 2021-02-19 | 南京莉上网络科技有限公司 | Battery sealing machine |
| CN114204060A (en) * | 2021-12-16 | 2022-03-18 | 深圳市远旺达科技有限公司 | Button cell is compaction equipment in batches |
Citations (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20020082729A (en) * | 2001-04-25 | 2002-10-31 | 에스케이씨 주식회사 | A button cell type lithium battery and its manufacturing method |
| CN1801503A (en) * | 2005-12-05 | 2006-07-12 | 天津工业大学 | Automatic sealing loader for button cell |
| DE102008017934A1 (en) * | 2007-04-19 | 2008-10-23 | Winsel, August, Prof. Dr.rer.nat. | Button cell generating hydrogen and electricity, includes porous layer saturated with paraffin oil, to form uni-directional gas seal for central vent hole |
| CN202333053U (en) * | 2011-11-18 | 2012-07-11 | 深圳市科晶智达科技有限公司 | Button cell sealing machine |
| CN203589152U (en) * | 2013-10-14 | 2014-05-07 | 甘肃大象能源科技有限公司 | A button lithium battery sealing machine |
| CN104325016A (en) * | 2014-10-08 | 2015-02-04 | 广东骏汇汽车科技股份有限公司 | One-step forming mold and one-step forming method of thick-material convex hull product |
| CN106784908A (en) * | 2016-12-28 | 2017-05-31 | 钦州市奥佳华新能源科技有限公司 | The closing device of button cell |
| CN206401435U (en) * | 2016-12-28 | 2017-08-11 | 钦州市奥佳华新能源科技有限公司 | The closing device of button cell |
| CN206849948U (en) * | 2017-04-10 | 2018-01-05 | 广州市特乐扩医疗器械有限公司 | A kind of lithium battery seal device |
| CN108232321A (en) * | 2018-03-02 | 2018-06-29 | 电子科技大学中山学院 | Lithium battery sealing device based on vacuum environment |
| CN208507852U (en) * | 2018-09-06 | 2019-02-15 | 鹏威机械(东莞)有限公司 | A kind of automatic sealer for buckle battery |
| CN209357852U (en) * | 2019-03-07 | 2019-09-06 | 郑州鼎能实业有限公司 | A kind of the pressure release handle and the hydraulic sealing machine of button cell of hydraulic sealing machine |
| CN209496962U (en) * | 2019-03-21 | 2019-10-15 | 郑州鼎能实业有限公司 | A kind of button cell sealing device |
| CN110350233A (en) * | 2019-07-30 | 2019-10-18 | 江西安驰新能源科技有限公司 | A kind of assembling of button cell and closing device |
| CN211208592U (en) * | 2020-03-17 | 2020-08-07 | 莆田新威邦电池有限公司 | Batch sealing device for button lithium batteries |
-
2020
- 2020-03-17 CN CN202010184362.6A patent/CN111342108B/en active Active
Patent Citations (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20020082729A (en) * | 2001-04-25 | 2002-10-31 | 에스케이씨 주식회사 | A button cell type lithium battery and its manufacturing method |
| CN1801503A (en) * | 2005-12-05 | 2006-07-12 | 天津工业大学 | Automatic sealing loader for button cell |
| DE102008017934A1 (en) * | 2007-04-19 | 2008-10-23 | Winsel, August, Prof. Dr.rer.nat. | Button cell generating hydrogen and electricity, includes porous layer saturated with paraffin oil, to form uni-directional gas seal for central vent hole |
| CN202333053U (en) * | 2011-11-18 | 2012-07-11 | 深圳市科晶智达科技有限公司 | Button cell sealing machine |
| CN203589152U (en) * | 2013-10-14 | 2014-05-07 | 甘肃大象能源科技有限公司 | A button lithium battery sealing machine |
| CN104325016A (en) * | 2014-10-08 | 2015-02-04 | 广东骏汇汽车科技股份有限公司 | One-step forming mold and one-step forming method of thick-material convex hull product |
| CN106784908A (en) * | 2016-12-28 | 2017-05-31 | 钦州市奥佳华新能源科技有限公司 | The closing device of button cell |
| CN206401435U (en) * | 2016-12-28 | 2017-08-11 | 钦州市奥佳华新能源科技有限公司 | The closing device of button cell |
| CN206849948U (en) * | 2017-04-10 | 2018-01-05 | 广州市特乐扩医疗器械有限公司 | A kind of lithium battery seal device |
| CN108232321A (en) * | 2018-03-02 | 2018-06-29 | 电子科技大学中山学院 | Lithium battery sealing device based on vacuum environment |
| CN208507852U (en) * | 2018-09-06 | 2019-02-15 | 鹏威机械(东莞)有限公司 | A kind of automatic sealer for buckle battery |
| CN209357852U (en) * | 2019-03-07 | 2019-09-06 | 郑州鼎能实业有限公司 | A kind of the pressure release handle and the hydraulic sealing machine of button cell of hydraulic sealing machine |
| CN209496962U (en) * | 2019-03-21 | 2019-10-15 | 郑州鼎能实业有限公司 | A kind of button cell sealing device |
| CN110350233A (en) * | 2019-07-30 | 2019-10-18 | 江西安驰新能源科技有限公司 | A kind of assembling of button cell and closing device |
| CN211208592U (en) * | 2020-03-17 | 2020-08-07 | 莆田新威邦电池有限公司 | Batch sealing device for button lithium batteries |
Non-Patent Citations (2)
| Title |
|---|
| 高新红 等: "转盘式纽扣电池快速封口机顶针断裂分析与改进设计", 《成都航空职业技术学院学报 》, vol. 33, no. 02, 19 June 2017 (2017-06-19), pages 40 - 42 * |
| 高新红;刘洋;: "转盘式纽扣电池快速封口机顶针断裂分析与改进设计", 成都航空职业技术学院学报, no. 02, 19 June 2017 (2017-06-19), pages 46 - 48 * |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111864163A (en) * | 2020-06-29 | 2020-10-30 | 江西新威动力能源科技有限公司 | Squeeze separator acid equipment with separator take-out mechanism |
| CN111864163B (en) * | 2020-06-29 | 2022-11-11 | 江西新威动力能源科技有限公司 | Partition plate extruding acid equipment with partition plate taking-out mechanism |
| CN112259779A (en) * | 2020-10-21 | 2021-01-22 | 深圳市合壹新能技术有限公司 | Packaging machine |
| CN112259779B (en) * | 2020-10-21 | 2021-12-10 | 深圳市合壹新能技术有限公司 | Packaging machine |
| CN112382770A (en) * | 2021-01-13 | 2021-02-19 | 南京莉上网络科技有限公司 | Battery sealing machine |
| CN112382770B (en) * | 2021-01-13 | 2021-06-25 | 南京莉上网络科技有限公司 | Battery sealing machine |
| CN114204060A (en) * | 2021-12-16 | 2022-03-18 | 深圳市远旺达科技有限公司 | Button cell is compaction equipment in batches |
| CN114204060B (en) * | 2021-12-16 | 2022-12-16 | 深圳市远旺达科技有限公司 | Button cell is compaction equipment in batches |
Also Published As
| Publication number | Publication date |
|---|---|
| CN111342108B (en) | 2025-03-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111342108B (en) | A batch sealing device for button lithium batteries | |
| CN110350233B (en) | Assembling and sealing device for button cell | |
| CN216228936U (en) | Hollow blade thimble hole processing frock | |
| CN209830023U (en) | End socket punch forming device | |
| WO2020173143A1 (en) | Hydrogen fuel cell packing device and packing method thereof | |
| CN211208592U (en) | Batch sealing device for button lithium batteries | |
| CN203386850U (en) | Shell stamping device of aluminum-plastic film of lithium battery | |
| CN210224194U (en) | Button cell's equipment and closing device | |
| CN212822046U (en) | Stamping device of aluminum product work piece | |
| CN211637970U (en) | Punching and bending device for portal frame assembly | |
| CN211588244U (en) | Stable single-punch die of unloading | |
| CN209880737U (en) | A press machine for static cavity of soft pack battery | |
| CN209439241U (en) | A kind of Pneumatic pressing device of the shell reparation for new-energy automobile lithium battery | |
| CN212190780U (en) | A button lithium battery metal lithium forming machine | |
| CN205008267U (en) | Concora crush test machine | |
| CN215299329U (en) | A kind of lead-acid battery into the tank equipment | |
| CN217990593U (en) | A punching device for the production of hardware accessories | |
| CN211758143U (en) | A secondary ejection structure for molds that is easy to demould | |
| CN208970677U (en) | A kind of two sealing mechanism of lithium ion battery | |
| CN209255583U (en) | Air-floating high-speed lithium battery pole piece punching die | |
| CN221496389U (en) | Perforating device is used in gasket processing | |
| CN217550891U (en) | A punching fixture for lithium battery production process | |
| CN219378676U (en) | High-efficiency combined stamping die | |
| CN222601009U (en) | Battery sealing equipment | |
| CN216581176U (en) | Punching machine for lithium battery aluminum plastic film |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |