Furniture manufacturing wooden board surface shaping treatment system
Technical Field
The invention relates to the technical field of plate processing, in particular to a furniture manufacturing wood plate surface shaping treatment system.
Background
The plate is used as a flat rectangular material plate, is widely applied to the building and furniture industries, and is mainly used as a component of a table, a chair, a ceiling or a wardrobe. In order to improve the use value of the plate, the surface of the plate is usually pasted with paper or sealed to beautify the appearance of the plate and protect the surface against scratches; after the surface of the plate is pasted with paper or sealed, the plate needs to be shaped by rolling or other methods, so that the plate is completely attached to the surface of the plate, and the flatness of the surface of the plate is ensured, but the following problems mainly exist in the shaping treatment process of the surface of the plate:
1. the existing method for shaping the surface of the plate by using equipment mainly extrudes the surface of the plate locally through a wood board or a heavy object, which easily causes the wrinkle of a sticker on the surface of the plate, the generation of bubbles or the upwarp of edges, and has poor shaping effect;
2. in the process of shaping the surface of the plate, the stress on the surface of the plate is uneven, so that the surface of the plate is damaged, and the plate side walls with different thicknesses can not be adjusted, so that the shaping treatment of the side walls of the plate is incomplete, and the normal use is influenced.
Disclosure of Invention
Technical problem to be solved
The invention can solve the problems that the existing method for shaping the surface of the plate by the equipment is mainly to locally extrude the surface of the plate by a wood plate or a heavy object, which is easy to cause the wrinkle of a sticker on the surface of the plate, generate bubbles or tilt the edge, and has poor shaping effect; and in the process of shaping the surface of the plate, the stress on the surface of the plate is uneven, so that the surface of the plate is damaged, and the plate side walls with different thicknesses can not be adjusted, so that the shaping treatment of the side walls of the plate is incomplete, the normal use is influenced, and the like.
(II) technical scheme
In order to achieve the purpose, the invention adopts the following technical scheme that the furniture manufacturing wooden board surface shaping processing system comprises a bottom plate, a fixed frame, a lower shaping module and an upper shaping module; a fixed frame is arranged above the bottom plate, a lower shaping module is arranged in the middle of the upper end of the bottom plate and is positioned in the fixed frame, and the upper shaping module is connected with the fixed frame and is positioned right above the lower shaping module; wherein:
the fixed frame comprises support columns, a top plate and adjusting cylinders, the support columns are uniformly installed on the bottom plate, the top plate is arranged at the upper ends of the support columns, and the adjusting cylinders are uniformly installed in the middle of the lower ends of the top plate.
The upper shaping module comprises an upper shaping seat, an upper rolling module, an upper connecting column, an upper limiting block, an adjusting screw, an adjusting head, a side roller and an upper buffer module; the upper shaping seats are respectively connected with adjusting cylinders on two sides below the top plate, the sections of the upper shaping seats are L-shaped, L-shaped chutes are formed in the upper shaping seats, an upper rolling module is installed in the L-shaped chutes between the two upper shaping seats, two ends of the upper rolling module are respectively connected with the upper limiting block through upper connecting columns, adjusting screws are evenly installed on the upper limiting block in a thread matching mode, adjusting heads are installed at the top ends of the adjusting screws, side rollers are installed at the bottom ends of the adjusting screws through bearings, and the upper buffering modules are evenly installed on the inner wall of the upper limiting block; according to the thickness of a plate to be processed, the upper shaping module is moved to a proper position through an adjusting cylinder, and the side rollers are moved downwards through a manual knob adjusting head, so that the bottoms of the side rollers are matched with the lower shaping module; the upper shaping module can adapt to surface shaping treatment of plates with different thicknesses, and the application range is expanded.
The upper rolling module comprises an actuating motor, a screw rod, a fixing plate, an upper sliding block, an upper fixing bracket and an upper roller; the actuating motor is arranged in the L-shaped sliding chute through a motor base, an output shaft of the actuating motor is connected with a shaft head at one end of the lead screw through a coupler, and a shaft head at the other end of the lead screw is connected with the fixing plate through a bearing; the fixing plate is arranged in the L-shaped sliding chute; the upper sliding blocks are arranged on the upper shaping base in a sliding fit mode and are connected with the lead screw in a thread fit mode, an upper fixing support is arranged between the two upper sliding blocks, and upper rollers are uniformly arranged on the upper fixing support through bearings; the lead screw is driven to rotate by the execution motor, so that the upper sliding block slides in the L-shaped sliding groove, the upper fixing support drives the upper roller to roll on the surface of the plate to be processed, and the upper limiting block is driven to slide in the L-shaped sliding groove by the upper connecting column, so that the side roller and the upper buffering module roll on the side wall of the plate to be processed; the upper buffer module is arranged to mainly extrude the corners of the board, and the raised positions of the corners of the board are shaped.
The upper buffering module comprises a U-shaped frame, a buffering spring and an auxiliary roller; the U-shaped frame is connected to the inner wall of the upper limiting block through a buffer spring, an auxiliary roller is arranged inside the U-shaped frame, and shaft heads at two ends of the auxiliary roller are connected with the U-shaped frame through bearings; the buffer spring who sets up makes supplementary roller laminate with the panel lateral wall all the time to the in-process of panel corner circulating rolling, has strengthened panel corner design treatment effect, and a plurality of supplementary rollers that set up roll extrusion simultaneously, have improved design treatment efficiency.
The lower shaping module comprises a lower shaping seat, a lower sliding block, a lower connecting column, a lower limiting block, a lower buffer module, a lower fixed bracket and a lower roller; the lower shaping seats are symmetrically arranged on the bottom plate and have the same structure as the upper shaping seat, a lower sliding block is arranged in an L-shaped sliding groove between the two lower shaping seats in a sliding fit mode, two ends of the lower sliding block are respectively connected with a lower limiting block through lower connecting columns, connecting holes are uniformly formed in the top end of the lower limiting block, balls are uniformly arranged in the connecting holes and are matched with side rollers, a lower buffering module is uniformly arranged on the inner wall of the lower limiting block, a lower fixing support is arranged between the two lower sliding blocks, lower rollers are uniformly arranged on the lower fixing support through bearings, and the lower buffering module and the upper buffering module have the same structure; when the rolling module slides in the actuating motor drive, through the mutual cooperation of side roller and lower stopper, the lower stopper of drive and the lower sliding block that connects slide in the L type spout of shaping seat down inside, and the roller rolls at the lower surface of panel under the drive, make lower roller and last roller carry out the roll extrusion to the panel surface in step, thereby form a rectangular frame and slide in the L type spout of last shaping seat and lower shaping seat, make in panel surface design processing procedure, wrap up it completely, the design quality on panel surface has been guaranteed.
Preferably, rubber pads are sleeved on the outer walls of the upper roller and the lower roller; the rubber pad can ensure that the stress on the surface of the plate is more uniform when the upper roller and the lower roller perform shaping treatment on the surface of the plate; on the other hand, the normal use of the plate can be prevented from being influenced by scratching the surface of the plate in the moving process of the upper roller and the lower roller.
Preferably, the inner wall of a connecting hole formed at the top end of the lower limiting block is uniformly provided with balls; the evenly arranged balls can reduce the friction of the side rollers when the side rollers rotate in the connecting holes, and the stability of the side rollers when the side rollers roll the side walls of the plates is ensured.
(III) advantageous effects
1. The executing motor drives the upper roller, the auxiliary roller, the side roller and the lower roller to synchronously roll the surface of the plate to be processed, so that a rectangular frame is formed to slide in the L-shaped sliding grooves of the upper shaping seat and the lower shaping seat, the plate is completely wrapped in the surface shaping process, the surface shaping processing efficiency of the plate is improved, and the flatness of the plate after shaping processing is ensured.
2. The buffer spring enables the auxiliary rollers to be always attached to the side walls of the plates in the process of circularly rolling the edges of the plates, so that the edges and corners of the plates are more firmly shaped, the shaping quality of the side walls of the plates is ensured, and the plurality of auxiliary rollers are simultaneously rolled, so that the shaping treatment efficiency is improved;
3. when the side roller is used for shaping the surface of the plate with different thicknesses, the side roller can extend out of the upper limiting block and is matched with the lower limiting block through the knob adjusting head, so that the neutral position of shaping the side wall of the plate is compensated, and the shaping treatment of the side wall of the plate is more comprehensive;
4. the rubber pad arranged in the invention can ensure that the stress on the surface of the plate is more uniform when the upper roller and the lower roller perform shaping treatment on the surface of the plate; on the other hand, the plate can be prevented from being scratched in the moving process of the upper roller and the lower roller, and the surface shaping treatment quality of the plate is ensured.
Drawings
The invention is further illustrated with reference to the following figures and examples.
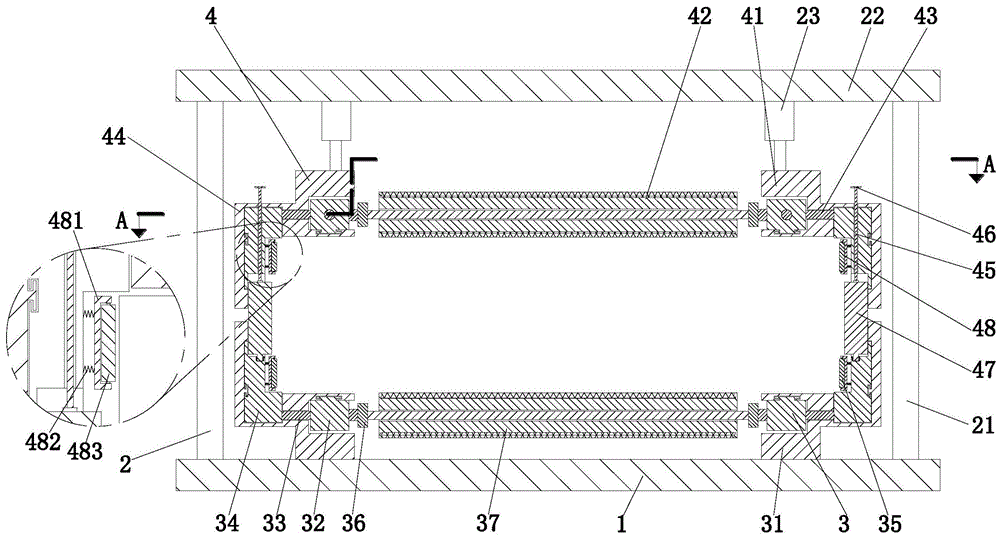
FIG. 1 is a front view in section view of the present invention;
FIG. 2 is a cross-sectional view taken along line A-A of FIG. 1 in accordance with the present invention;
fig. 3 is a schematic view of the working state of the present invention.
Detailed Description
Embodiments of the present invention will be described below with reference to the drawings. In this process, the width of the lines or the size of the components in the drawings may be exaggerated for clarity and convenience of description.
The following terms are defined based on the functions of the present invention, and may be different depending on the intention of the user or the operator or the convention. Therefore, these terms are defined based on the entire contents of the present specification.
As shown in fig. 1 to 3, a surface sizing treatment system for a wooden board for furniture manufacture comprises a base plate 1, a fixing frame 2, a lower sizing module 3 and an upper sizing module 4; a fixed frame 2 is arranged above the bottom plate 1, a lower shaping module 3 is arranged in the middle of the upper end of the bottom plate 1, the lower shaping module 3 is positioned in the fixed frame 2, and an upper shaping module 4 is connected with the fixed frame 2 and is positioned right above the lower shaping module 3; wherein: fixed frame 2 include support column 21, roof 22 and adjusting cylinder 23, support column 21 evenly install on bottom plate 1, the upper end of support column 21 is provided with roof 22, adjusting cylinder 23 is evenly installed in roof 22 lower extreme middle part.
The upper sizing module 4 comprises an upper sizing seat 41, an upper rolling module 42, an upper connecting column 43, an upper limiting block 44, an adjusting screw 45, an adjusting head 46, a side roller 47 and an upper buffer module 48; the upper shaping seats 41 are respectively connected with the adjusting cylinders 23 on two sides below the top plate 22, the sections of the upper shaping seats 41 are L-shaped, L-shaped sliding grooves are formed in the upper shaping seats 41, an upper rolling module 42 is installed in the L-shaped sliding grooves between the two upper shaping seats 41, two ends of the upper rolling module 42 are respectively connected with an upper limiting block 44 through upper connecting columns 43, adjusting screws 45 are evenly installed on the upper limiting block 44 in a thread matching mode, adjusting heads 46 are installed at the top ends of the adjusting screws 45, side rollers 47 are installed at the bottom ends of the adjusting screws 45 through bearings, and upper buffering modules 48 are evenly installed on the inner wall of the upper limiting block 44; according to the thickness of the plate to be processed, the upper shaping module 4 is moved to a proper position through the adjusting cylinder 23, and the side rollers 47 are moved downwards through the manual knob adjusting head 46, so that the bottoms of the side rollers are matched with the lower shaping module 3; the upper shaping module 4 can adapt to surface shaping treatment of plates with different thicknesses, and the application range is expanded; the upper rolling module 42 comprises an actuating motor 421, a lead screw 422, a fixed plate 423, an upper sliding block 424, an upper fixed bracket 425 and an upper roller 426; the actuating motor 421 is installed in the L-shaped chute through a motor base, an output shaft of the actuating motor 421 is connected with a shaft head at one end of the screw 422 through a coupling, and a shaft head at the other end of the screw 422 is connected with the fixing plate 423 through a bearing; the fixing plate 423 is arranged in the L-shaped sliding groove; the upper sliding blocks 424 are arranged on the upper shaping base 41 in a sliding fit manner and are connected with the screw 422 in a thread fit manner, an upper fixing bracket 425 is arranged between the two upper sliding blocks 424, and upper rollers 426 are uniformly arranged on the upper fixing bracket 425 through bearings; the actuating motor 421 drives the screw 422 to rotate, so that the upper sliding block 424 slides in the L-shaped chute, the upper fixing bracket 425 drives the upper roller 426 to roll on the surface of the plate to be processed, and the upper connecting column 43 drives the upper limiting block 44 to slide in the L-shaped chute, so that the side roller 47 and the upper buffering module 48 roll on the side wall of the plate to be processed; the arranged upper buffer module 48 is mainly used for extruding the corners of the board and shaping the raised parts of the corners of the board; the upper buffer module 48 comprises a U-shaped frame 481, a buffer spring 482 and an auxiliary roller 483; the U-shaped frame 481 is connected to the inner wall of the upper limit block 44 through a buffer spring 482, an auxiliary roller 483 is arranged inside the U-shaped frame 481, and shaft heads at two ends of the auxiliary roller 483 are connected with the U-shaped frame 481 through bearings; buffer spring 482 who sets up makes supplementary roller 483 laminate with the panel lateral wall all the time to the in-process that panel corner circulated roll extrusion, has strengthened panel corner design treatment effect, and a plurality of supplementary rollers 483 that set up roll extrusion simultaneously, has improved design treatment effeciency.
The lower shaping module 3 comprises a lower shaping seat 31, a lower sliding block 32, a lower connecting column 33, a lower limiting block 34, a lower buffer module 35, a lower fixing bracket 36 and a lower roller 37; lower type seat 31 symmetry install on bottom plate 1, and it is the looks isostructure with last type seat 41, be located two L type spouts between the type seat 31 down inside and install down sliding block 32 through the sliding fit mode, the both ends of down sliding block 32 are connected with stopper 34 down through lower spliced pole 33 respectively, the connecting hole has evenly been seted up on stopper 34 top down, and the connecting hole cooperatees with side roller 47, evenly be provided with down buffer module 35 on the inner wall of stopper 34 down, lower buffer module 35 and last buffer module 48 be the isostructure. A lower fixed bracket 36 is arranged between the two lower sliding blocks 32, and lower rollers 37 are uniformly arranged on the lower fixed bracket 36 through bearings; when the execution motor 421 drives the upper rolling module 42 to slide, the side rollers 47 and the lower limiting block 34 are mutually matched to drive the lower limiting block 34 and the lower sliding block 32 connected with the lower limiting block to slide in the L-shaped sliding groove of the lower shaping base 31 and drive the lower roller 37 to roll on the lower surface of the plate, so that the lower roller 37 and the upper roller 426 synchronously roll on the surface of the plate, thereby forming a rectangular frame which slides in the L-shaped sliding grooves of the upper shaping base 41 and the lower shaping base 31, completely wrapping the plate in the plate surface shaping process, and ensuring the shaping quality of the surface of the plate; rubber pads are sleeved on the outer walls of the upper roller 426 and the lower roller 37; the rubber pads are arranged, so that the stress on the surface of the plate is more uniform when the upper rollers 426 and the lower rollers 37 perform shaping treatment on the surface of the plate; on the other hand, the normal use of the plate can be prevented from being influenced by scratching the surface of the plate in the moving process of the upper roller 426 and the lower roller 37; the inner wall of a connecting hole formed in the top end of the lower limiting block 34 is uniformly provided with balls; the evenly arranged balls can reduce the friction of the side rollers 47 when the side rollers 47 rotate in the connecting holes, and the stability of the side rollers 47 when the side rollers 47 roll the side walls of the plates is ensured.
When in work; firstly, a plate to be shaped is placed on the lower shaping seat 31, and the upper shaping module 4 is moved to a proper position through the adjusting cylinder 23, so that the upper roller 426 is in contact with the upper surface of the plate to be shaped;
then, the side roller 47 is matched with the lower limit block 34 by turning the adjusting head 46, and the actuating motor 421 is started to drive the upper sliding block 424 to slide in the L-shaped sliding groove of the upper shaping base 41, so as to drive the upper roller 426, the side roller 47, the auxiliary roller 483 and the lower roller 37 to synchronously roll on the outer wall of the plate;
and finally, taking down and stacking the plates subjected to surface shaping treatment.
The above description is only a preferred embodiment of the present invention and is not intended to limit the present invention, and various modifications and changes may be made by those skilled in the art. Any modification, equivalent replacement, or improvement made within the spirit and principle of the present invention should be included in the protection scope of the present invention.