CN108746318B - Lithium battery cutting mold automatic lubrication device - Google Patents
Lithium battery cutting mold automatic lubrication device Download PDFInfo
- Publication number
- CN108746318B CN108746318B CN201810875102.6A CN201810875102A CN108746318B CN 108746318 B CN108746318 B CN 108746318B CN 201810875102 A CN201810875102 A CN 201810875102A CN 108746318 B CN108746318 B CN 108746318B
- Authority
- CN
- China
- Prior art keywords
- oil
- knife
- punching
- storage tank
- knife edge
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000005520 cutting process Methods 0.000 title claims abstract description 16
- 238000005461 lubrication Methods 0.000 title claims abstract description 14
- WHXSMMKQMYFTQS-UHFFFAOYSA-N Lithium Chemical compound [Li] WHXSMMKQMYFTQS-UHFFFAOYSA-N 0.000 title claims abstract description 12
- 229910052744 lithium Inorganic materials 0.000 title claims abstract description 12
- 238000004080 punching Methods 0.000 claims abstract description 36
- 238000003860 storage Methods 0.000 claims abstract description 20
- 230000001050 lubricating effect Effects 0.000 claims abstract description 8
- 239000007788 liquid Substances 0.000 claims abstract description 6
- 238000002347 injection Methods 0.000 claims description 23
- 239000007924 injection Substances 0.000 claims description 23
- 229910000851 Alloy steel Inorganic materials 0.000 claims description 3
- 230000000694 effects Effects 0.000 abstract description 4
- 239000003921 oil Substances 0.000 description 57
- 239000002699 waste material Substances 0.000 description 8
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 7
- 239000000446 fuel Substances 0.000 description 7
- 229910052782 aluminium Inorganic materials 0.000 description 5
- 239000010687 lubricating oil Substances 0.000 description 5
- HBBGRARXTFLTSG-UHFFFAOYSA-N Lithium ion Chemical compound [Li+] HBBGRARXTFLTSG-UHFFFAOYSA-N 0.000 description 2
- 229910001416 lithium ion Inorganic materials 0.000 description 2
- 238000012423 maintenance Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 230000002035 prolonged effect Effects 0.000 description 2
- 238000010008 shearing Methods 0.000 description 2
- 239000000243 solution Substances 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- YWXYYJSYQOXTPL-SLPGGIOYSA-N isosorbide mononitrate Chemical compound [O-][N+](=O)O[C@@H]1CO[C@@H]2[C@@H](O)CO[C@@H]21 YWXYYJSYQOXTPL-SLPGGIOYSA-N 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 229910052751 metal Inorganic materials 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 239000007774 positive electrode material Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D28/00—Shaping by press-cutting; Perforating
- B21D28/02—Punching blanks or articles with or without obtaining scrap; Notching
- B21D28/14—Dies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D37/00—Tools as parts of machines covered by this subclass
- B21D37/18—Lubricating, e.g. lubricating tool and workpiece simultaneously
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Battery Electrode And Active Subsutance (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
Abstract
本发明公开了锂电池裁切模具全自动润滑装置,包括冲刀,所述冲刀设置在刀口内,且所述刀口设置在下刀座的一侧,所述冲刀通过固定孔固定在下刀座上,且所述冲刀设置在刀口内的一拐角处设有定位凸块,所述定位凸块固定在定位槽内,所述定位槽设置在下刀座靠近冲刀的一侧面板上,所述下刀座外侧设有若干输油管,所述输油管的一端通过分流槽道与刀口连通,所述输油管远离刀口的一端连接有气动节流阀。所述气动节流阀通过输油管连接有储油罐,所述储油罐上端设有加油孔和压缩气入口,且所述储油罐内设有液位传感器,本发明结构简单,使用方便,可以提高冲刀与刀口之间的润滑效果,可以清洁冲刀,增加刀模的使用寿命。
The invention discloses a full-automatic lubricating device for a lithium battery cutting die, comprising a punching knife, the punching knife is arranged in the knife edge, and the knife edge is set on one side of the lower knife seat, and the punching knife is fixed on the lower knife seat through a fixing hole , and the punching knife is set at a corner of the knife edge with a positioning bump, the positioning bump is fixed in the positioning groove, and the positioning groove is set on the side panel of the lower knife seat close to the punching knife, so A number of oil delivery pipes are arranged outside the lower knife seat, one end of the oil delivery pipe communicates with the knife edge through a flow diversion channel, and the end of the oil delivery pipe away from the knife edge is connected with a pneumatic throttle valve. The pneumatic throttle valve is connected to an oil storage tank through an oil delivery pipe, and the upper end of the oil storage tank is provided with a refueling hole and a compressed gas inlet, and a liquid level sensor is provided in the oil storage tank. The present invention is simple in structure and easy to use. It can improve the lubrication effect between the punching knife and the knife edge, clean the punching knife and increase the service life of the knife die.
Description
技术领域:Technical field:
本发明属于锂离子电池正极片冲切设备技术领域,特别涉及锂电池裁切模具全自动润滑装置。The invention belongs to the technical field of punching equipment for positive electrode sheets of lithium-ion batteries, and in particular relates to a full-automatic lubricating device for lithium-ion battery cutting molds.
背景技术:Background technique:
新能源汽车日益普及,电池的性能关系着新能源汽车的里程,特别是电池的安全性能,尤为重要,而目前国内主流动力铝壳多极耳电芯,极耳制作工艺多采用五金模具冲压成型,由于正极材料的特性,刀具容易粘铝屑,冲切时间久了,极耳容易产生毛刺,废料也容易粘在刀口,导致润滑效果变差,冲切的精度降低,形成二次剪切,在产品极耳上粘连头发丝类的废料,对后期制成的成品电芯带来了极大的安全隐患,因此急需一种能够提高刀口润滑效果的措施,从而解决刀口粘铝的问题,提高冲压模具的使用寿命,所以本发明提供锂电池裁切模具全自动润滑装置来实现通过在模具刀口增加喷油润滑装置,保证刀口润湿,同时通过润滑油液自动带走刀口上的废料,保证刀口不沾铝屑,保证冲切精度,延长模具使用寿命的功能。New energy vehicles are becoming more and more popular, and the performance of the battery is related to the mileage of the new energy vehicle, especially the safety performance of the battery, which is particularly important. At present, the domestic mainstream power aluminum shell multi-tab battery, the tab production process mostly uses metal mold stamping forming , due to the characteristics of the positive electrode material, the tool is easy to stick to aluminum chips. After a long time of punching, the tabs are prone to burrs, and the waste is also easy to stick to the edge of the knife, resulting in poor lubrication, reduced punching accuracy, and secondary shearing. Sticking hair-like waste on the product tabs has brought great safety hazards to the finished battery cells made in the later stage. Therefore, there is an urgent need for a measure that can improve the lubrication effect of the knife edge, so as to solve the problem of aluminum sticking on the knife edge and improve The service life of the stamping die, so the present invention provides a lithium battery cutting die automatic lubrication device to achieve by adding an oil spray lubrication device to the die edge to ensure that the edge is wet, and at the same time, the waste on the edge is automatically taken away by the lubricating oil to ensure The knife edge does not stick to aluminum chips, which ensures punching accuracy and prolongs the service life of the mold.
发明内容:Invention content:
本发明的目的就在于为了解决上述问题而提供锂电池裁切模具全自动润滑装置,解决了现有的锂电池裁切模具刀具容易粘铝屑,冲切时间久了,极耳容易产生毛刺,废料也容易粘在刀口,导致润滑效果变差,冲切的精度降低,形成二次剪切,在产品极耳上粘连头发丝类的废料,对后期制成的成品电芯带来了极大的安全隐患的缺点。The purpose of the present invention is to provide a full-automatic lubricating device for lithium battery cutting dies in order to solve the above problems, which solves the problem that existing lithium battery cutting dies are prone to sticking to aluminum scraps, and the tabs are prone to burrs after punching for a long time. The waste material is also easy to stick to the knife edge, resulting in poor lubrication effect, lower punching precision, forming secondary shearing, and sticking hair-like waste materials on the product tabs, which has brought great harm to the finished battery cells made in the later stage. The disadvantages of security risks.
为了解决上述问题,本发明提供了一种技术方案:In order to solve the above problems, the present invention provides a technical solution:
一种锂电池裁切模具全自动润滑装置,包括冲刀和下刀座,所述下刀座的一侧设有与冲刀配合的刀口,所述冲刀通过固定孔固定在下刀座上方的上模板上,且所述冲刀朝向刀口一侧的一拐角处设有定位凸块,所述刀口的侧壁设有与定位凸块对应的定位槽,所述下刀座外侧设有若干输油管,所述输油管的一端通过分流槽道与刀口连通,所述冲刀面向刀口的一侧设有与分流槽道对应的导流槽道,所述导流槽道弧形向上延伸,并且上端设有两个喷油口,所述两个喷油口的喷油方向对称分布于分流槽道进油方向的两侧,并且所述喷油口与同一导流槽道的进油口位于冲刀的同一侧,所述输油管远离刀口的一端连接有气动节流阀,所述气动节流阀通过输油管连接有储油罐,所述储油罐上端设有加油孔和压缩气入口,且所述储油罐内设有液位传感器。A fully automatic lubricating device for a lithium battery cutting die, comprising a punching knife and a lower knife seat, one side of the lower knife seat is provided with a knife edge matched with the punching knife, and the punching knife is fixed on the top of the lower knife seat through a fixing hole On the upper template, a positioning bump is provided at a corner of the punching knife facing the side of the knife edge, a positioning groove corresponding to the positioning bump is provided on the side wall of the knife edge, and a number of oil delivery pipes are provided on the outside of the lower knife seat , one end of the oil delivery pipe communicates with the knife edge through the diversion channel, and the side of the punching knife facing the knife edge is provided with a diversion channel corresponding to the diversion channel, and the diversion channel extends upward in an arc shape, and the upper end is provided with There are two oil injection ports, and the injection directions of the two oil injection ports are symmetrically distributed on both sides of the oil inlet direction of the diversion channel, and the oil injection port and the oil inlet port of the same diversion channel are located on the punching knife On the same side of the oil delivery pipe, the end of the oil delivery pipe away from the knife edge is connected to a pneumatic throttle valve, and the pneumatic throttle valve is connected to an oil storage tank through the oil delivery pipeline. A liquid level sensor is arranged in the oil storage tank.
作为优选,所述加油孔内设有单通阀。Preferably, a one-way valve is provided in the oil filling hole.
作为优选,所述下刀座的下方设有接油槽以及驱动接油槽前后移动的气缸,所述接油槽上设有滤网,所述接油槽内设有回流管,所述回流管与储油罐连接。As a preference, an oil receiving tank and a cylinder for driving the oil receiving tank to move forward and backward are provided under the lower tool seat, a filter screen is provided on the oil receiving tank, and a return pipe is provided in the oil receiving tank, and the return pipe and the oil storage tank connection.
作为优选,所述压缩气入口与外置的空气压缩机连通,且压缩气压力控制为3kg。Preferably, the compressed air inlet is connected to an external air compressor, and the pressure of the compressed air is controlled to be 3kg.
作为优选,所述加油孔上端口安装有孔盖。Preferably, the upper port of the oil filling hole is equipped with a hole cover.
作为优选,所述储油罐的壳体由合金钢制成。Preferably, the shell of the oil storage tank is made of alloy steel.
作为优选,所述喷油口的喷油方向倾斜向下设置。Preferably, the fuel injection direction of the fuel injection port is arranged obliquely downward.
本发明的有益效果:Beneficial effects of the present invention:
锂电池裁切模具全自动润滑装置,通过在下刀座上设置连通到刀口处的进油通道,通过控制冲切过程中的进油情况,保证冲切过程刀口的润滑效果,使得刀模使用保养频次明显下降,刀口粘铝粉的现象基本解决,刀模的使用寿命也明显加长,同时也降低了由于刀口粘废料而导致二次剪切带;通过在冲刀上设置与分流槽道对应的导流槽道,并使导流槽道弧形向上延伸后设置两个喷油口,从而增加润滑油的喷油范围,提高润滑效果;本发明结构简单,使用方便,可以清洁冲刀,增加刀模的使用寿命。油路喷油量通过程序设定时间和节流阀调节控制,储油罐带液位传感器,使用到下线位自动报警,提醒加油。The automatic lubrication device of the lithium battery cutting die ensures the lubrication effect of the cutting edge by setting the oil inlet channel connected to the cutting edge on the lower knife seat and controlling the oil feeding situation during the punching process, so that the use and maintenance of the cutting die The frequency is significantly reduced, the phenomenon of sticking aluminum powder on the knife edge is basically solved, and the service life of the knife die is also significantly prolonged. At the same time, it also reduces the secondary shear band caused by the sticky waste on the knife edge; diversion channel, and after extending the diversion channel arc upwards, two oil injection ports are set, thereby increasing the range of lubricating oil injection and improving the lubricating effect; The service life of the knife die. The fuel injection volume of the oil circuit is controlled by the program setting time and throttle valve adjustment, and the oil storage tank is equipped with a liquid level sensor, which will automatically alarm when it is used to the lower line level, reminding to refuel.
附图说明:Description of drawings:
为了易于说明,本发明由下述的具体实施及附图作以详细描述。For ease of illustration, the present invention is described in detail by the following specific implementations and accompanying drawings.
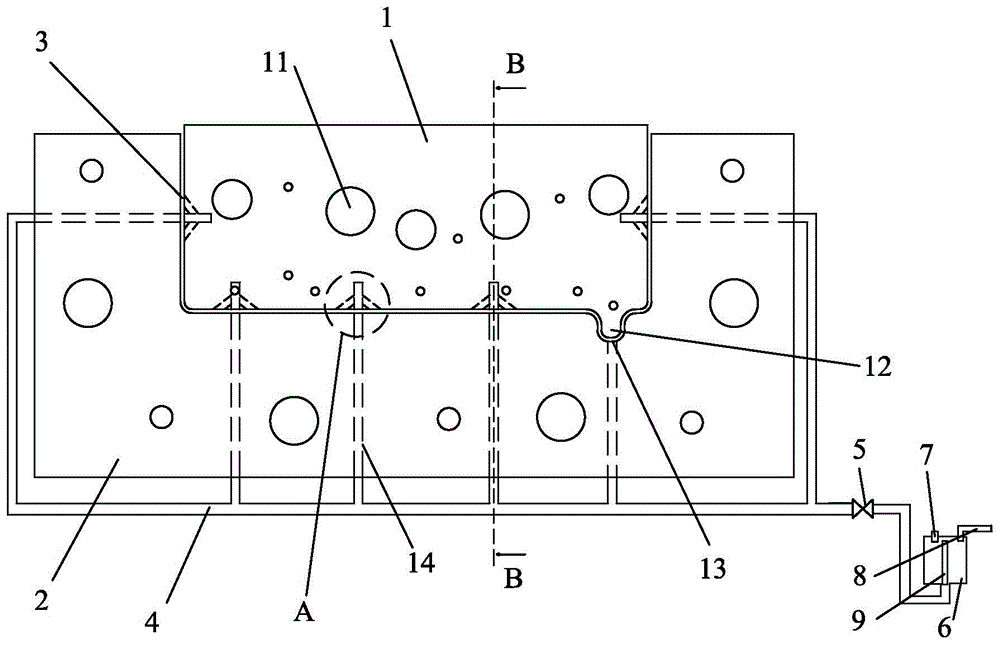
图1为本发明之实施例的组装结构俯视图;Fig. 1 is the assembly structure plan view of the embodiment of the present invention;
图2为本发明之实施例的组装结构侧视图;Fig. 2 is the side view of the assembled structure of the embodiment of the present invention;
图3为图1中B-B处的截面示意图;Fig. 3 is a schematic cross-sectional view at B-B in Fig. 1;
图4为图1中A处的放大示意图。FIG. 4 is an enlarged schematic view of point A in FIG. 1 .
图中:1、冲刀;2、下刀座;3、刀口;4、输油管;5、气动节流阀;6、储油罐;7、加油孔;8、压缩气入口;9、液位传感器;10、接油槽;11、固定孔;12、定位凸块;13、定位槽;14、分流槽道;15、导流槽道;16、喷油口;17、滤网;18、回流管。In the figure: 1, punching knife; 2, lower knife seat; 3, knife edge; 4, oil delivery pipe; 5, pneumatic throttle valve; 6, oil storage tank; 7, oil filling hole; 8, compressed air inlet; 9, liquid level Sensor; 10, oil receiving groove; 11, fixing hole; 12, positioning bump; 13, positioning groove; 14, diversion channel; 15, diversion channel; 16, fuel injection port; Tube.
具体实施方式:Detailed ways:
如图1-4所示,本具体实施方式采用以下技术方案:As shown in Figures 1-4, this embodiment adopts the following technical solutions:
一种锂电池裁切模具全自动润滑装置,包括冲刀1和下刀座2,所述下刀座2的一侧设有与冲刀1配合的刀口3,所述冲刀1通过固定孔11固定在下刀座2上方的上模板上,且所述冲刀1朝向刀口3一侧的一拐角处设有定位凸块12,所述刀口3的侧壁设有与定位凸块12对应的定位槽13,所述下刀座2外侧设有若干输油管4,所述输油管4的一端通过分流槽道14与刀口3连通,所述冲刀1面向刀口3的一侧设有与分流槽道14对应的导流槽道15,所述导流槽道15弧形向上延伸,并且上端设有两个喷油口16,所述两个喷油口16的喷油方向对称分布于分流槽道进油方向的两侧,并且所述喷油口16与同一导流槽道15的进油口位于冲刀1的同一侧,所述输油管4远离刀口3的一端连接有气动节流阀5,所述气动节流阀5通过输油管4连接有储油罐6,所述储油罐6上端设有加油孔7和压缩气入口8,且所述储油罐6内设有液位传感器9。所述加油孔7内设有单通阀,以防止储油罐6内加压后润滑油回流的情况出现。A fully automatic lubricating device for a lithium battery cutting die, comprising a
具体的,所述下刀座2的下方设有接油槽10以及驱动接油槽前后移动的气缸,所述接油槽10上设有滤网17,所述接油槽10内设有回流管18,所述回流管18与储油罐6连接。具体的,所述压缩气入口8与外置的空气压缩机连通,且压缩气压力控制为3kg。其压力使得清洗油的流出速度稳定且不会出现过量的情况,由实践数据得出。Specifically, an oil receiving
具体的,所述加油孔7上端口安装有孔盖,以防止尘屑掉落进加油孔7内。Specifically, a hole cover is installed on the upper port of the
具体的,所述储油罐6的壳体由合金钢制成,以确保其在内部高压的环境下不会轻易出现形变,且防止电池废料对其产生腐蚀。Specifically, the shell of the oil storage tank 6 is made of alloy steel to ensure that it will not be easily deformed in an internal high-pressure environment, and to prevent corrosion of the battery waste.
具体的,所述喷油口16的喷油方向倾斜向下设置,从而提高冲切产品的杂物的清除效率。Specifically, the oil injection direction of the
本发明工作原理如下:The working principle of the present invention is as follows:
当需要对模具进行润滑时,气缸驱动接油槽10移动至下刀座2的下方,润滑油经加压后,通过输油管4输送到分流槽道14,然后由分流槽道14喷入导流槽道15,再经由导流槽道15的两个喷油口16喷出,从而实现对刀口3及刀口3内的冲刀进行润滑,同时对刀口3内的杂物进行清洗,自刀口3入流下的润滑油通过滤网17过滤后由接油槽10进行回收利用,润滑完成后,接油槽10由气缸驱动移动,重新进行材料的冲切。该设计通过使用喷油润滑装置后,刀模使用保养频次明显下降,刀口粘铝粉的现象基本解决,刀模的使用寿命也明显加长,同时也降低了由于刀口粘废料而导致二次剪切带,本发明结构简单,使用方便,可以清洁冲刀,增加刀模的使用寿命。When the mold needs to be lubricated, the cylinder drives the
以上显示和描述了本发明的基本原理和主要特征和本发明的优点,本行业的技术人员应该了解,本发明不受上述实施例的限制,上述实施例和说明书中描述的只是说明本发明的原理,在不脱离本发明精神和范围的前提下,本发明还会有各种变化和改进,这些变化和改进都落入要求保护的本发明范围内,本发明要求保护范围由所附的权利要求书及其等效物界定。Above shows and described basic principle of the present invention and main feature and the advantage of the present invention, those skilled in the art should understand that, the present invention is not limited by above-mentioned embodiment, and what described in above-mentioned embodiment and description just illustrates the present invention Principle, under the premise of not departing from the spirit and scope of the present invention, the present invention also has various changes and improvements, and these changes and improvements all fall within the claimed scope of the present invention, and the claimed scope of the present invention is defined by the appended claims Requirements and their equivalents are defined.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201810875102.6A CN108746318B (en) | 2018-08-03 | 2018-08-03 | Lithium battery cutting mold automatic lubrication device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201810875102.6A CN108746318B (en) | 2018-08-03 | 2018-08-03 | Lithium battery cutting mold automatic lubrication device |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN108746318A CN108746318A (en) | 2018-11-06 |
| CN108746318B true CN108746318B (en) | 2023-06-23 |
Family
ID=63968632
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201810875102.6A Active CN108746318B (en) | 2018-08-03 | 2018-08-03 | Lithium battery cutting mold automatic lubrication device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN108746318B (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111331038A (en) * | 2020-04-07 | 2020-06-26 | 江苏尚诚精密模具科技有限公司 | Washing machine box forming die |
| CN114309249B (en) * | 2021-12-22 | 2024-02-20 | 长沙矿冶研究院有限责任公司 | Lithium sheet die cutting method |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101386047A (en) * | 2007-09-14 | 2009-03-18 | 法因图尔知识产权股份公司 | Method and device for lubricating a tool and workpiece when cutting |
| CN201558912U (en) * | 2009-12-23 | 2010-08-25 | 张家港金鸿顺机械工业有限公司 | Self-lubrication punching die |
| CN103056233A (en) * | 2012-11-19 | 2013-04-24 | 江苏大学 | Fog-lubrication method and device of high-speed stamping die |
| JP2013081968A (en) * | 2011-10-06 | 2013-05-09 | Aisin Seiki Co Ltd | Mold device |
| CN203843023U (en) * | 2014-04-03 | 2014-09-24 | 勤钦精密工业(昆山)有限公司 | Automatic in-mould greasing and lubricating device |
| CN206083645U (en) * | 2016-07-20 | 2017-04-12 | 成都瑞垚电子有限公司 | Automatic oil feeding structure in mould |
| CN206912080U (en) * | 2017-06-12 | 2018-01-23 | 昆山维开安电子科技有限公司 | The punching press mode structure to be refueled in mould |
| CN207043189U (en) * | 2017-06-15 | 2018-02-27 | 东莞市睿信机电科技有限公司 | Lubrication structure of stamping die for power battery case |
| CN207154517U (en) * | 2017-09-22 | 2018-03-30 | 东莞致宏精密模具有限公司 | A kind of high-precision die cutting die |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN208483087U (en) * | 2018-08-03 | 2019-02-12 | 东莞致宏精密模具有限公司 | Lithium battery cutting mould full automatic lubricating device |
-
2018
- 2018-08-03 CN CN201810875102.6A patent/CN108746318B/en active Active
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101386047A (en) * | 2007-09-14 | 2009-03-18 | 法因图尔知识产权股份公司 | Method and device for lubricating a tool and workpiece when cutting |
| CN201558912U (en) * | 2009-12-23 | 2010-08-25 | 张家港金鸿顺机械工业有限公司 | Self-lubrication punching die |
| JP2013081968A (en) * | 2011-10-06 | 2013-05-09 | Aisin Seiki Co Ltd | Mold device |
| CN103056233A (en) * | 2012-11-19 | 2013-04-24 | 江苏大学 | Fog-lubrication method and device of high-speed stamping die |
| CN203843023U (en) * | 2014-04-03 | 2014-09-24 | 勤钦精密工业(昆山)有限公司 | Automatic in-mould greasing and lubricating device |
| CN206083645U (en) * | 2016-07-20 | 2017-04-12 | 成都瑞垚电子有限公司 | Automatic oil feeding structure in mould |
| CN206912080U (en) * | 2017-06-12 | 2018-01-23 | 昆山维开安电子科技有限公司 | The punching press mode structure to be refueled in mould |
| CN207043189U (en) * | 2017-06-15 | 2018-02-27 | 东莞市睿信机电科技有限公司 | Lubrication structure of stamping die for power battery case |
| CN207154517U (en) * | 2017-09-22 | 2018-03-30 | 东莞致宏精密模具有限公司 | A kind of high-precision die cutting die |
Also Published As
| Publication number | Publication date |
|---|---|
| CN108746318A (en) | 2018-11-06 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201558912U (en) | Self-lubrication punching die | |
| CN108746318A (en) | Lithium battery cutting mould full automatic lubricating device | |
| CN211218308U (en) | Anti-adsorption type car interior panel stamping die | |
| CN208483087U (en) | Lithium battery cutting mould full automatic lubricating device | |
| CN208084796U (en) | A foam automatic molding machine | |
| CN206673041U (en) | Lithium ion power cell pole flakes edge foil gluing membrane module | |
| CN211707923U (en) | Automatic stamping die of oiling | |
| CN203039017U (en) | Accumulator efficient acid discharge system | |
| CN203739120U (en) | Centralized feeding device for injection molding | |
| CN208450415U (en) | A kind of accurate Refuel structure of mold | |
| CN206405303U (en) | A kind of progressive die automatic oil feeding device | |
| CN207549261U (en) | A kind of rubber production pours device | |
| CN203925470U (en) | Glass tube oil gauge device | |
| CN206236755U (en) | Simple aluminum-shell lithium battery negative pressure formation device | |
| CN204954488U (en) | Saponified oil of cast panel machine cutter device that oils | |
| CN203670063U (en) | Anti-freezing crude oil filter | |
| CN202622212U (en) | Pneumatic spot welding machine system capable of preventing water channel icing | |
| CN209696315U (en) | For suction port of compressor lime set moving-out device in sulfuric acid process alkylation process | |
| CN203835485U (en) | Engine oil strainer | |
| CN208696071U (en) | A mold automatic chip removal and dust removal device | |
| CN202244815U (en) | Lower cone bottom oil storage tank | |
| CN202250398U (en) | Oil collecting tank | |
| CN210887438U (en) | Novel no negative pressure automatic water supply equipment | |
| CN106627110A (en) | Large truck fuel tank | |
| CN202226648U (en) | Oil pipe connector |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| CB03 | Change of inventor or designer information | ||
| CB03 | Change of inventor or designer information |
Inventor after: Fu Haimin Inventor after: Chen Yanmei Inventor before: Fu Haiming Inventor before: Chen Yanmei |
|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address | ||
| CP03 | Change of name, title or address |
Address after: Room 101, Building 1, 1888 Meiling West Road, Dalang Town, Dongguan City, Guangdong Province 523000 Patentee after: DONGGUAN ZHIHONG PRECISION MOULD CO.,LTD. Country or region after: China Address before: Jiekou Village, Chang'an Town, Dongguan City, Guangdong Province, 523000 Patentee before: DONGGUAN ZHIHONG PRECISION MOULD CO.,LTD. Country or region before: China |