CN103722718A - PEEK plastic rod production device and process - Google Patents
PEEK plastic rod production device and process Download PDFInfo
- Publication number
- CN103722718A CN103722718A CN201310738099.0A CN201310738099A CN103722718A CN 103722718 A CN103722718 A CN 103722718A CN 201310738099 A CN201310738099 A CN 201310738099A CN 103722718 A CN103722718 A CN 103722718A
- Authority
- CN
- China
- Prior art keywords
- temperature
- minutes
- section
- peek
- machine
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 239000004696 Poly ether ether ketone Substances 0.000 title claims abstract description 38
- JUPQTSLXMOCDHR-UHFFFAOYSA-N benzene-1,4-diol;bis(4-fluorophenyl)methanone Chemical compound OC1=CC=C(O)C=C1.C1=CC(F)=CC=C1C(=O)C1=CC=C(F)C=C1 JUPQTSLXMOCDHR-UHFFFAOYSA-N 0.000 title claims abstract description 38
- 229920002530 polyetherether ketone Polymers 0.000 title claims abstract description 38
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 27
- 238000000034 method Methods 0.000 title claims abstract description 11
- 239000004033 plastic Substances 0.000 title abstract description 10
- 238000001125 extrusion Methods 0.000 claims abstract description 37
- 238000005520 cutting process Methods 0.000 claims abstract description 32
- 238000010438 heat treatment Methods 0.000 claims abstract description 28
- 238000007493 shaping process Methods 0.000 claims abstract description 12
- 238000001035 drying Methods 0.000 claims abstract description 10
- 230000005540 biological transmission Effects 0.000 claims abstract description 5
- 238000001816 cooling Methods 0.000 claims description 21
- 239000000463 material Substances 0.000 claims description 17
- 230000006835 compression Effects 0.000 claims description 13
- 238000007906 compression Methods 0.000 claims description 13
- 239000002994 raw material Substances 0.000 claims description 10
- 238000000265 homogenisation Methods 0.000 claims description 9
- 229910000831 Steel Inorganic materials 0.000 claims description 8
- 239000010959 steel Substances 0.000 claims description 8
- 239000000155 melt Substances 0.000 claims description 7
- 238000004513 sizing Methods 0.000 claims description 7
- 239000000498 cooling water Substances 0.000 claims description 6
- 238000002844 melting Methods 0.000 claims description 6
- 230000008018 melting Effects 0.000 claims description 6
- 238000005516 engineering process Methods 0.000 claims description 5
- 235000012438 extruded product Nutrition 0.000 claims description 5
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 2
- 239000011505 plaster Substances 0.000 claims 7
- 238000000465 moulding Methods 0.000 claims 3
- 235000021050 feed intake Nutrition 0.000 claims 2
- 238000007789 sealing Methods 0.000 claims 1
- 238000004321 preservation Methods 0.000 abstract description 4
- 238000003825 pressing Methods 0.000 abstract description 4
- 239000000203 mixture Substances 0.000 description 4
- 239000012768 molten material Substances 0.000 description 4
- 230000007423 decrease Effects 0.000 description 3
- 238000009413 insulation Methods 0.000 description 3
- 239000011148 porous material Substances 0.000 description 3
- 238000010521 absorption reaction Methods 0.000 description 2
- 238000005452 bending Methods 0.000 description 2
- 239000003638 chemical reducing agent Substances 0.000 description 2
- 239000011347 resin Substances 0.000 description 2
- 229920005989 resin Polymers 0.000 description 2
- 230000007812 deficiency Effects 0.000 description 1
- 239000008187 granular material Substances 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000010008 shearing Methods 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/90—Thermal treatment of the stream of extruded material, e.g. cooling with calibration or sizing, i.e. combined with fixing or setting of the final dimensions of the extruded article
- B29C48/908—Thermal treatment of the stream of extruded material, e.g. cooling with calibration or sizing, i.e. combined with fixing or setting of the final dimensions of the extruded article characterised by calibrator surface, e.g. structure or holes for lubrication, cooling or venting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/53—Screws having a varying channel depth, e.g. varying the diameter of the longitudinal screw trunk
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/03—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor characterised by the shape of the extruded material at extrusion
- B29C48/06—Rod-shaped
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/03—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor characterised by the shape of the extruded material at extrusion
- B29C48/09—Articles with cross-sections having partially or fully enclosed cavities, e.g. pipes or channels
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/395—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die using screws surrounded by a cooperating barrel, e.g. single screw extruders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/625—Screws characterised by the ratio of the threaded length of the screw to its outside diameter [L/D ratio]
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/78—Thermal treatment of the extrusion moulding material or of preformed parts or layers, e.g. by heating or cooling
- B29C48/875—Thermal treatment of the extrusion moulding material or of preformed parts or layers, e.g. by heating or cooling for achieving a non-uniform temperature distribution, e.g. using barrels having both cooling and heating zones
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/90—Thermal treatment of the stream of extruded material, e.g. cooling with calibration or sizing, i.e. combined with fixing or setting of the final dimensions of the extruded article
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/91—Heating, e.g. for cross linking
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/911—Cooling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/919—Thermal treatment of the stream of extruded material, e.g. cooling using a bath, e.g. extruding into an open bath to coagulate or cool the material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/92—Measuring, controlling or regulating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C71/00—After-treatment of articles without altering their shape; Apparatus therefor
- B29C71/02—Thermal after-treatment
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2793/00—Shaping techniques involving a cutting or machining operation
- B29C2793/0027—Cutting off
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92504—Controlled parameter
- B29C2948/92561—Time, e.g. start, termination, duration or interruption
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92504—Controlled parameter
- B29C2948/9258—Velocity
- B29C2948/9259—Angular velocity
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92504—Controlled parameter
- B29C2948/92704—Temperature
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92819—Location or phase of control
- B29C2948/92857—Extrusion unit
- B29C2948/92876—Feeding, melting, plasticising or pumping zones, e.g. the melt itself
- B29C2948/92885—Screw or gear
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92819—Location or phase of control
- B29C2948/92857—Extrusion unit
- B29C2948/92876—Feeding, melting, plasticising or pumping zones, e.g. the melt itself
- B29C2948/92895—Barrel or housing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2948/00—Indexing scheme relating to extrusion moulding
- B29C2948/92—Measuring, controlling or regulating
- B29C2948/92819—Location or phase of control
- B29C2948/92923—Calibration, after-treatment or cooling zone
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/001—Combinations of extrusion moulding with other shaping operations
- B29C48/0022—Combinations of extrusion moulding with other shaping operations combined with cutting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/885—External treatment, e.g. by using air rings for cooling tubular films
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/90—Thermal treatment of the stream of extruded material, e.g. cooling with calibration or sizing, i.e. combined with fixing or setting of the final dimensions of the extruded article
- B29C48/905—Thermal treatment of the stream of extruded material, e.g. cooling with calibration or sizing, i.e. combined with fixing or setting of the final dimensions of the extruded article using wet calibration, i.e. in a quenching tank
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/88—Thermal treatment of the stream of extruded material, e.g. cooling
- B29C48/911—Cooling
- B29C48/9115—Cooling of hollow articles
- B29C48/912—Cooling of hollow articles of tubular films
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
Abstract
本发明公开了一种PEEK塑料棒生产设备及工艺。设备包括主机和辅机,所述主机为一台挤出机,它包括挤压系统、转动系统、控制系统;所述挤压系统为炮筒螺杆;所述转动系统包括电机和减速箱;所述控制系统包括电器仪表和执行机构;所述辅机包括模具、牵引机、油温机、切割机、烤箱;所述模具包括主模、导流板、隔热圈、成型定型筒以及冷却水箱;所述油温机安装在成型管的定型段;所述牵引机主要包括传动装置、辊筒压紧装置和刹车制动装置,它安装在保温装置的后面;所述切割机安装在模具出口后面;所述烤箱为密封的箱体;工艺包括投料、烘干、塑化挤出、均化分流、成型/定型、牵引、切板/堆料、热处理。
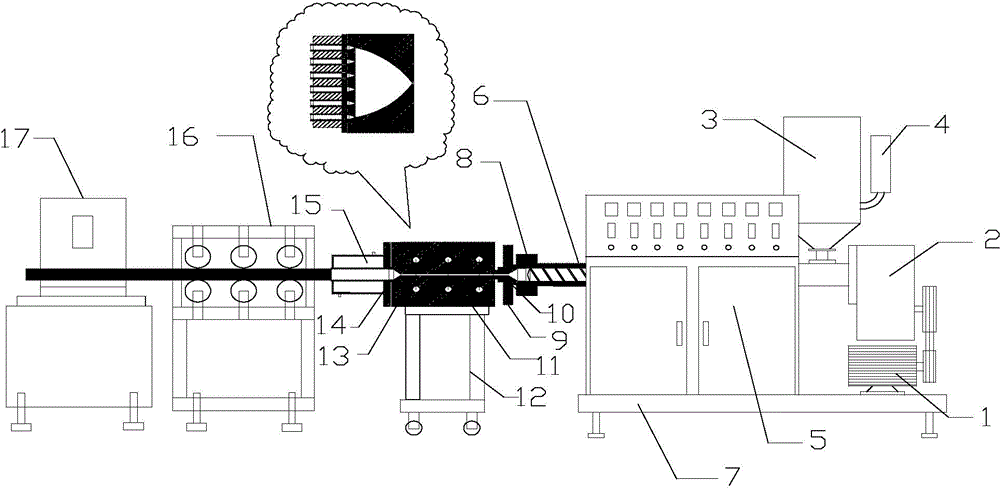
The invention discloses a PEEK plastic rod production equipment and process. The equipment includes a main machine and an auxiliary machine. The main machine is an extruder, which includes an extrusion system, a rotating system, and a control system; the extrusion system is a barrel screw; the rotating system includes a motor and a reduction box; The control system includes electrical instruments and actuators; the auxiliary machine includes molds, tractors, oil temperature machines, cutting machines, and ovens; ; The oil temperature machine is installed in the shaping section of the forming pipe; the tractor mainly includes a transmission device, a roller pressing device and a brake device, which is installed behind the heat preservation device; the cutting machine is installed in the mold outlet The latter; the oven is a sealed box; the process includes feeding, drying, plasticizing and extruding, homogenizing and splitting, forming/setting, traction, cutting board/stacking, and heat treatment.
Description
技术领域technical field
本发明公开了一种PEEK塑料棒生产设备及工艺。The invention discloses a PEEK plastic rod production equipment and process.
背景技术Background technique
PEEK棒挤出成型是把粒状物料由料斗加入到挤出机的机筒内,物料在螺杆旋转的挤压推动作用下,通过机筒内壁和螺杆表面的摩擦作用向前输送和压实,通过机筒外部的加热装置和摩擦预热,在高温、高压条件下熔融塑化。然后,连续转动的螺杆再把熔融物料推入机头模具,从机头模具挤出的熔融物料经冷却定型成为所需的PEEK制品。PEEK rod extrusion molding is to add granular materials into the barrel of the extruder from the hopper, and the materials are conveyed forward and compacted by the friction between the inner wall of the barrel and the surface of the screw under the extrusion force of the screw rotation. The heating device and friction preheating on the outside of the barrel melt and plasticize under high temperature and high pressure conditions. Then, the continuously rotating screw pushes the molten material into the mold of the die, and the molten material extruded from the die is cooled and shaped into the required PEEK product.
以前生产设备和工艺如下:The previous production equipment and process are as follows:
PEEK棒挤出成型生产线图1所示,PEEK棒挤出机成型生产线的组成:PEEK rod extrusion molding production line is shown in Figure 1, the composition of the PEEK rod extrusion molding production line:
PEEK棒挤出的生产线由主机、辅机两部分组成,这些部分称为挤出机组。其中主机为一台挤出机,由以下三部分组成:挤压系统、转动系统、控制系统。挤压系统为炮筒螺杆,采用专用等距渐变型PEEK挤出螺杆,螺杆长径比为30:1,压缩比为3。转动系统主要由电机和减速箱组成。电机运转,通过皮带传动带动减速箱,从而使螺杆保持一定的剪切速率。挤出机的控制系统主要电器仪表和执行机构组成,其主要作用是控制主机,使其操作的转速和功率正常,并保证主机和辅机的温度、压力、流量和制品的质量,实现全机组的自动控制。辅机:挤出机的组成是根据制品的种类而定的,一般辅机由下列几部分组成:单棒模具、牵引机、切割装置。模具:模具由法兰、机头体、定形筒、冷却水箱组装而成;熔融的原料在螺杆旋转剪切的作用下进入机头体,通过喇叭口,在一定压力将螺旋融料转为直线型进入成型筒成型,在冷却水的作用下凝固、定型。牵引机主要由传动装置、辊筒压紧装置和刹车制动装置组成;安装在保温装置的后面,通过连杆将模具与牵引机固定在一起,气控制牵引机上下4对辊压紧板材,减速机拖动辊筒使制品在压缩区保持一定压力匀速前进。切割机为棒材切割设备,安装在管材模具出口后面,挤出的制品穿过切割机的切割支撑面,通过锯片的高速旋转切割棒材,切成所需要的长度。The production line of PEEK rod extrusion consists of two parts, the main machine and the auxiliary machine, which are called extrusion units. The main machine is an extruder, which consists of the following three parts: extrusion system, rotation system and control system. The extrusion system is a barrel screw, using a special equidistant gradual PEEK extrusion screw, the screw length-to-diameter ratio is 30:1, and the compression ratio is 3. The rotating system is mainly composed of a motor and a gearbox. The motor runs, and the reduction box is driven by the belt drive, so that the screw maintains a certain shear rate. The control system of the extruder is mainly composed of electrical instruments and actuators. Its main function is to control the main machine to make its operating speed and power normal, and to ensure the temperature, pressure, flow and product quality of the main machine and auxiliary machines, so as to realize the whole unit. automatic control. Auxiliary machine: The composition of the extruder depends on the type of product. Generally, the auxiliary machine consists of the following parts: single rod die, tractor, and cutting device. Mold: The mold is assembled by the flange, the head body, the shaping cylinder, and the cooling water tank; the molten raw material enters the head body under the action of the screw rotating and shearing, and turns the spiral molten material into a straight line under a certain pressure through the bell mouth. The mold enters the forming cylinder to be formed, solidified and shaped under the action of cooling water. The tractor is mainly composed of a transmission device, a roller pressing device and a brake device; it is installed behind the heat preservation device, and the mold and the tractor are fixed together through a connecting rod. The reducer drives the roller to keep the product at a certain pressure in the compression zone and move forward at a constant speed. The cutting machine is a bar cutting equipment, which is installed behind the outlet of the pipe mold. The extruded product passes through the cutting support surface of the cutting machine, cuts the bar through the high-speed rotation of the saw blade, and cuts it into the required length.
挤出成型的生产工艺过程为:投料→烘干→塑化挤出→成型/定型→牵引→切割/堆放。The production process of extrusion molding is: feeding → drying → plasticizing extrusion → forming/setting → traction → cutting/stacking.
⑴投料:及时投料,保证料斗不空。不同的料不能混用,注意分清料的牌号及料的类型,防止杂物、杂料进入料斗,造成下料口堵塞。⑴Feeding: Feed in time to ensure that the hopper is not empty. Different materials cannot be mixed. Pay attention to distinguish the grade and type of materials to prevent sundries and miscellaneous materials from entering the hopper and causing blockage of the discharge port.
⑵烘干:由于PEEK树脂吸温性较大,在挤出成型前必须经进干燥处理,排除水份,否则其水份含量超过一定限度,水份就会在挤出机筒内挥发成气体,使制品内部含有气孔,和强度下降。采用130℃循环热风对PEEK料进行干燥,干燥时间为4-6H,使产品内的水份含量低于0.2%。⑵Drying: Due to the high temperature absorption of PEEK resin, it must be dried before extrusion molding to remove moisture, otherwise its moisture content exceeds a certain limit, and the moisture will evaporate into gas in the extruder barrel , so that the product contains pores inside, and the strength decreases. Use 130°C circulating hot air to dry the PEEK material, the drying time is 4-6H, so that the moisture content in the product is less than 0.2%.
⑶塑化挤出:通过机筒温度与螺杆的作用,物料转变为具有一定流动性的均匀连续熔体被挤出的过程。分三区对机筒加温,根据原材料特性设定温度:一区加料段温度:380-390℃;二区融熔压缩段温度:390-400℃;三区均化段温度:390-400℃;接头:390-400℃;挤出螺杆速度:4-6r/min。(3) Plasticizing extrusion: through the action of barrel temperature and screw, the material is transformed into a uniform and continuous melt with certain fluidity and extruded. The barrel is heated in three zones, and the temperature is set according to the characteristics of the raw materials: the temperature of the feeding section in the first zone: 380-390°C; the temperature in the melting and compression section in the second zone: 390-400°C; ℃; Joint: 390-400℃; Extrusion screw speed: 4-6r/min.
⑷成型/定型:具有流动性的均匀熔体,由于螺杆的旋转挤压通过多孔板进入模具,并按一定形状的型胚成型、定型后被挤出模具。①模具压缩区分为四区进行恒温,便熔体保持一定黏度成型,即:机头体温度:320-330℃;②在模具冷却定型区的两端都接有冷却循环水,通过冷水的不断循环使熔料的温度不断降低,最后凝固结晶定型被挤出模具。⑷Forming/Sizing: The uniform melt with fluidity enters the mold through the perforated plate due to the rotary extrusion of the screw, and is formed and shaped according to a certain shape of the parison and then extruded out of the mold. ①The mold compression zone is divided into four zones for constant temperature, so that the melt can be molded with a certain viscosity, that is, the temperature of the head body: 320-330°C; ②Cooling circulating water is connected to both ends of the cooling and shaping zone of the mold. The circulation makes the temperature of the molten material decrease continuously, and finally solidifies and crystallizes and is extruded out of the mold.
⑸牵引:通过牵引机拖动PEEK棒,使棒材在恒压状态下匀速前进,保证产品质量的稳定性。⑸Traction: The PEEK rod is dragged by the tractor to make the rod move forward at a constant speed under constant pressure to ensure the stability of product quality.
⑹切割/堆料:用卷尺测出1000MM长度,启动切割机,切出所需要的长度,将棒材整齐叠放在特定的堆料架上。在棒与棒层之间放有不锈方钢,层与层之间的方钢上下看起来最好在一条直线上。⑹Cutting/Stacking: Use a tape measure to measure the length of 1000MM, start the cutting machine, cut out the required length, and stack the bars neatly on a specific stacking rack. There is a stainless square steel between the rod and the rod layer, and the square steel between the layers looks best to be in a straight line up and down.
存在问题有:1、棒材表面花斑、黑圈;2、表面浪痕、刮伤;3、内部黄芯;4、棒材颜色偏黄;5、机械性能差;6、棒材弯曲严重;7、生产效率低。Existing problems include: 1. Spots and black circles on the surface of the bar; 2. Wave marks and scratches on the surface; 3. Yellow core inside; 4. The color of the bar is yellowish; 5. Poor mechanical properties; 6. Serious bending of the bar ; 7, low production efficiency.
发明内容Contents of the invention
本发明的目的是克服现有技术的不足,提供一种PEEK塑料棒生产设备及工艺。The purpose of the invention is to overcome the deficiencies in the prior art, and provide a kind of PEEK plastic rod production equipment and technology.
为了实现上述目的,本发明采用如下技术方案:In order to achieve the above object, the present invention adopts the following technical solutions:
一种PEEK塑料棒生产设备,包括主机和辅机,所述主机为一台挤出机,它包括挤压系统、转动系统、控制系统;所述挤压系统为炮筒螺杆;所述转动系统包括电机和减速箱;所述包括控制系统包括电器仪表和执行机构;所述辅机包括模具、牵引机、油温机、切割机、烤箱;所述模具包括主模、导流板、隔热圈、成型定型筒以及冷却水箱;所述油温机安装在成型管的定型段;所述牵引机主要包括传动装置、辊筒压紧装置和刹车制动装置,它安装在保温装置的后面;所述切割机安装在模具出口后面;所述烤箱为密封的箱体。A kind of PEEK plastic bar production equipment, comprises main engine and auxiliary machine, and described main engine is an extruder, and it comprises extruding system, rotating system, control system; Described extruding system is barrel screw; Described rotating system It includes a motor and a gearbox; the control system includes electrical instruments and actuators; the auxiliary machine includes a mold, tractor, oil temperature machine, cutting machine, oven; the mold includes a main mold, deflector, heat insulation ring, forming and calibrating cylinder and cooling water tank; the oil temperature machine is installed in the calibrating section of the forming pipe; the tractor mainly includes a transmission device, a roller pressing device and a braking device, which is installed in the back of the heat preservation device; The cutting machine is installed behind the mold outlet; the oven is a sealed box.
进一步地,所述挤压系统采用专用等距渐变型PEEK挤出螺杆,螺杆长径比为30:1,压缩比为3。Further, the extrusion system uses a dedicated equidistant gradual PEEK extrusion screw with a screw length-to-diameter ratio of 30:1 and a compression ratio of 3.
进一步地,所述切割机为棒材切割设备。Further, the cutting machine is bar cutting equipment.
本发明的另一目的在于提供一种PEEK塑料棒生产工艺,包括:Another object of the present invention is to provide a kind of PEEK plastic rod production technique, comprising:
投料:及时投料,保证料斗不空,不同的料不能混用;Feeding: Feed in time to ensure that the hopper is not empty, and different materials cannot be mixed;
烘干:采用130℃循环热风对PEEK进行干燥,干燥时间为4-6H,使产品内的水份含量低于0.2%;Drying: Use 130°C circulating hot air to dry PEEK, the drying time is 4-6H, so that the moisture content in the product is less than 0.2%;
塑化挤出:通过机筒温度与螺杆的作用,物料转变为具有一定流动性的均匀连续熔体被挤出的过程;Plasticizing extrusion: through the action of barrel temperature and screw, the material is transformed into a uniform and continuous melt with certain fluidity and extruded;
均化分流:具有流动性的均匀熔体,由于螺杆的旋转挤压通过多孔板进入主模,融体在主模内进一步均化且将融料由螺旋运动转为直线运动;Homogenization and diversion: the uniform melt with fluidity, due to the rotary extrusion of the screw, enters the main mold through the perforated plate, the melt is further homogenized in the main mold and the melt is changed from spiral motion to linear motion;
成型/定型:①直线流动的熔体,由主模出口被均匀流入导流板,通过导流板的V型槽进行分流,分别进入多棒成型模的成型管,在成型管内成型;导流板均化温度为300℃;②在成型管的定型箱体两端装有油温机,在高温状态下定型,保证制品能够顺利被挤出和表面光洁度;定型温度为150-180℃;Forming/Sizing: ①The straight-line flowing melt is evenly flowed into the deflector from the outlet of the main mold, diverted through the V-shaped groove of the deflector, and enters the forming tube of the multi-rod forming mold respectively, and is formed in the forming tube; The homogenization temperature of the plate is 300°C; ②The oil temperature machine is installed at both ends of the shaping box of the forming tube, and the shape is shaped at a high temperature to ensure that the product can be extruded smoothly and the surface is smooth; the shaping temperature is 150-180°C;
牵引:在模具的出口位置装有刹车座,通过刹车座调节刹车条的松紧而夹紧板材制品,使熔融的原料在压缩区形成一定的压力,使挤出产品的结构紧密;Traction: A brake seat is installed at the exit of the mold, and the plate product is clamped by adjusting the tightness of the brake bar through the brake seat, so that the molten raw material forms a certain pressure in the compression zone, so that the structure of the extruded product is tight;
切板/堆料:用卷尺测出1000MM长度,启动切割机,切出所需要的长度,将棒材整齐叠放在特定的堆料架上。在棒与棒层之间放有不锈方钢,层与层之间的方钢上下看起来最好在一条直线上;Cutting/Stacking: Use a tape measure to measure the length of 1000MM, start the cutting machine, cut out the required length, and stack the bars neatly on a specific stacking rack. There is a stainless square steel between the rod and the rod layer, and the square steel between the layers looks best in a straight line;
热处理:对叠放堆好的PEEK棒进行热处理。Heat treatment: Heat treatment of stacked PEEK rods.
进一步地,所述塑化挤出分三区对机筒加温,根据原材料特性设定温度:一区加料段温度:355-370℃;二区融熔压缩段温度:360-380℃;三区均化段温度:360-380℃;接头:370-390℃;挤出螺杆速度:8-10r/min。Further, the plasticizing extrusion is divided into three zones to heat the barrel, and the temperature is set according to the characteristics of the raw materials: the temperature of the feeding section in the first zone: 355-370°C; the temperature in the melting and compression section of the second zone: 360-380°C; Zone homogenization section temperature: 360-380°C; Joint: 370-390°C; Extrusion screw speed: 8-10r/min.
进一步地,所述均化分流过程中,融体均化保持温度,即主模设定温度为:前一区温度为330-340℃;前二区温度为330-340℃;后一区温度为330-340℃;后二区温度为330-340℃。Further, in the process of homogenization and splitting, the melt homogenization maintenance temperature, that is, the set temperature of the main mold is: the temperature of the first zone is 330-340°C; the temperature of the first two zones is 330-340°C; the temperature of the latter zone is 330-340°C; It is 330-340°C; the temperature in the second zone is 330-340°C.
进一步地,所述热处理分为十六段:Further, the heat treatment is divided into sixteen sections:
第一段加温温度40℃ 升温时间20分钟The first heating temperature is 40°C and the heating time is 20 minutes
第二段恒温温度70℃ 恒温时间90分钟The second constant temperature temperature is 70°C and the constant temperature time is 90 minutes
第三段加温温度70℃ 加温时间20分钟The third heating temperature is 70°C and the heating time is 20 minutes
第四段恒温温度100℃ 恒温时间90分钟The fourth section of constant temperature temperature 100 ℃ constant temperature time 90 minutes
第五段加温温度100℃ 加温时间20分钟The fifth heating temperature is 100°C and the heating time is 20 minutes
第六段恒温温度120℃ 恒温时间90分钟The sixth stage constant temperature temperature is 120°C and the constant temperature time is 90 minutes
第七段加温温度120℃ 加温时间20分钟The heating temperature of the seventh stage is 120°C and the heating time is 20 minutes
第八段恒温温度150℃ 恒温时间厚度*2*30分钟The eighth section constant temperature temperature 150 ℃ constant temperature time thickness * 2 * 30 minutes
第九段降温温度150℃ 降温时间20分钟The ninth stage cooling temperature is 150°C and the cooling time is 20 minutes
第十段恒温温度120℃ 恒温时间180分钟The tenth section constant temperature temperature is 120°C and the constant temperature time is 180 minutes
第十一段降温温度120℃ 降温时间20分钟The cooling temperature of the eleventh stage is 120°C and the cooling time is 20 minutes
第十二段恒温温度100℃ 恒温时间180分钟The twelfth section constant temperature temperature 100 ℃ constant temperature time 180 minutes
第十三段降温温度100℃ 降温时间20分钟The thirteenth section cooling temperature 100 ℃ cooling time 20 minutes
第十四段恒温温度70℃ 怛温时间180分钟The fourteenth section constant temperature temperature is 70°C and the temperature time is 180 minutes
第十五段降温温度70℃ 降温时间20分钟The cooling temperature of the fifteenth section is 70°C and the cooling time is 20 minutes
第十六段恒温温度40℃ 温时间180分钟。The sixteenth stage constant temperature temperature is 40°C and the temperature time is 180 minutes.
由于采用了上述方案,消除了产品表面的轻微花斑和黑圈,使得产品表面光滑,流痕和刮伤的现象大大减少;同时,其机械性能满足要求,棒材内应力消除,不会有弯曲的现象,棒材内部无气孔、黄线,生产效率还得到了很大的提高。Due to the adoption of the above scheme, the slight spots and black circles on the surface of the product are eliminated, making the surface of the product smooth, and the phenomenon of flow marks and scratches is greatly reduced; at the same time, its mechanical properties meet the requirements, and the internal stress of the bar is eliminated, and there will be no There is no bending phenomenon, there are no pores and yellow lines inside the bar, and the production efficiency has also been greatly improved.
附图说明Description of drawings
图1是本发明实施例提供的PEEK塑料棒生产设备的结构示意图;Fig. 1 is the structural representation of the PEEK plastic rod production equipment that the embodiment of the present invention provides;
图2是本发明实施例提供的PEEK塑料棒生产工艺流程图;Fig. 2 is the PEEK plastic rod production process flowchart that the embodiment of the present invention provides;
其中:1、电机;2、减速箱;3、料斗;4、烤箱;5、控制系统;6、炮筒螺杆;7、机架;8、法兰;9、连接四方板;10、进料口;11、主模;12、模具架;13、导流板;14、隔热圈;15、冷却水箱;16、牵引机;17、切割机。Among them: 1. Motor; 2. Gear box; 3. Hopper; 4. Oven; 5. Control system; 6. Barrel screw; 7. Rack; 8. Flange; 9. Connecting square plate; 10. Feeding 11, main mold; 12, mold frame; 13, deflector; 14, heat insulation ring; 15, cooling water tank; 16, traction machine; 17, cutting machine.
具体实施方式Detailed ways
以下结合附图对本发明的实施例进行详细说明,但是本发明可以由权利要求限定和覆盖的多种不同方式实施。The embodiments of the present invention will be described in detail below with reference to the accompanying drawings, but the present invention can be implemented in many different ways defined and covered by the claims.
如图1-2所示,本实施例提供了一种PEEK塑料棒生产设备,PEEK棒挤出机成型生产线的组成,PEEK挤出的生产线包括主机、辅机,这些部分称为挤出机组;其中主机是一台挤出机,它包括挤压系统、转动系统、控制系统;挤压系统为炮筒螺杆6,采用专用等距渐变型PEEK挤出螺杆,螺杆长径比为30:1,压缩比为3;转动系统包括电机1和减速箱2,电机1运转,通过皮带传动带动减速箱2,从而使螺杆保持一定的剪切速率;挤出机的控制系统5包括电器仪表和执行机构,其主要作用是控制主机,使其操作的转速和功率正常,并保证主机和辅机的温度、压力、流量和制品的质量,实现全机组的自动控制;电机1、减速箱2、控制系统5、料斗3和烤箱设在机架7上;辅机:挤出机的组成是根据制品的种类而定的,一般辅机由下列几部分组成:模具、牵引机、油温机、切割机、烤箱4;模具包括主模11、导流板13、隔热圈14、成型定型筒、冷却水箱15、法兰8;模具设在模具架12上;进料口10靠近主模11侧设有连接四方板9,熔融的原料通过进料口10进入主模,进流道分流挡块两边进行分流,经过分流的熔融原料在一定的压力下进入导流板八个喇叭口和成型筒,在一定的压力和油温恒温定型的状态下成型、定型;油温机安装在成型管的定型段,通过热油不断循环,使定型区制品在恒定均衡的温度下定型并顺利挤出模具;牵引机16主要由传动装置、辊筒压紧装置和刹车制动装置组成。安装在保温装置的后面,通过连杆将模具与牵引机固定在一起,气控制牵引机上下4对辊压紧板材,减速机拖动辊筒使制品在压缩区保持一定压力匀速前进;切割机17为棒材切割设备,安装在模具出口后面,挤出的制品穿过切割机的切割支撑面,通过锯片的高速旋转切割棒材,切成所需要的长度制品;烤箱为密封的箱体,通过温度控制器,设定不同温度,不同时间多段对制品进行热处理,消除制品残余内应力,保证产品质量和稳定性。As shown in Figure 1-2, the present embodiment provides a kind of PEEK plastic rod production equipment, the composition of PEEK rod extruder forming production line, the production line of PEEK extruding includes main engine, auxiliary machine, and these parts are called extruder unit; The main engine is an extruder, which includes extrusion system, rotation system, and control system; the extrusion system is barrel screw 6, which adopts a special equidistant gradual PEEK extrusion screw, and the length-to-diameter ratio of the screw is 30:1. The compression ratio is 3; the rotation system includes a motor 1 and a gear box 2, and the motor 1 runs and drives the gear box 2 through a belt drive, so that the screw maintains a certain shear rate; the control system 5 of the extruder includes electrical instruments and actuators , its main function is to control the main engine so that its operating speed and power are normal, and to ensure the temperature, pressure, flow and product quality of the main engine and auxiliary equipment, so as to realize the automatic control of the whole unit; motor 1, gearbox 2, control system 5. The
本发明的另一目的在于提供了一种PEEK塑料棒生产工艺,挤出成型的生产工艺过程包括:投料、烘干、塑化挤出、均化分流、成型/定型、牵引、切板/堆料、热处理。⑴投料:及时投料,保证料斗不空.不同的料不能混用,注意分清料的牌号及料的类型,防止杂物、杂料进入料斗,造成下料口堵塞。⑵烘干:由于PEEK树脂吸温性较大,在挤出成型前必须经进干燥处理,排除水份,否则其水份含量超过一定限度,水份就会在挤出机筒内挥发成气体,使制品内部含有气孔,和强度下降;采用130℃循环热风对PEEK进行干燥,干燥时间为4-6H,使产品内的水份含量低于0.2%。⑶塑化挤出:通过机筒温度与螺杆的作用,物料转变为具有一定流动性的均匀连续熔体被挤出的过程;分三区对机筒加温,根据原材料特性设定温度:一区加料段温度:355-370℃;二区融熔压缩段温度:360-380℃;三区均化段温度:360-380℃;接头:370-390℃;挤出螺杆速度:8-10r/min。⑷均化分流:具有流动性的均匀熔体,由于螺杆的旋转挤压通过多孔板进入主模,融体在主模内进一步均化且将融料由螺旋运动转为直线运动:①融体均化保持温度,即主模设定温度:前一区温度:330-340℃;前二区温度:330-340℃;后一区温度:330-340℃后二区温度:330-340℃。⑸成型/定型:①直线流动的熔体,由主模出口被均匀流入导流板,通过导流板的V型槽进行分流,分别进入多棒成型模的成型管,在成型管内成型;导流板均化温度:300℃;②在成型管的定型箱体两端装有油温机,在高温状态下定型,保证制品能够顺利被挤出和表面光洁度;定型温度:150-180℃。⑹牵引装置:在模具的出口位置装有刹车座,通过刹车座调节刹车条的松紧而夹紧板材制品,使熔融的原料在压缩区形成一定的压力,使挤出产品的结构紧密。⑺切板/堆料:用卷尺测出1000MM长度,启动切割机,切出所需要的长度,将棒材整齐叠放在特定的堆料架上。在棒与棒层之间放有不锈方钢,层与层之间的方钢上下看起来最好在一条直线上。⑻烤箱热处理:对叠放堆好的PEEK棒进行热处理时,主要分为十六段:Another object of the present invention is to provide a production process for PEEK plastic rods. The production process of extrusion molding includes: feeding, drying, plasticizing extrusion, homogenizing and splitting, forming/setting, traction, cutting boards/stacking material, heat treatment. ⑴ Feeding: Feed in time to ensure that the hopper is not empty. Different materials cannot be mixed, pay attention to distinguish the grade and type of materials, and prevent sundries and miscellaneous materials from entering the hopper, causing the discharge port to be blocked. ⑵Drying: Due to the high temperature absorption of PEEK resin, it must be dried before extrusion molding to remove moisture, otherwise its moisture content exceeds a certain limit, and the moisture will evaporate into gas in the extruder barrel , so that the inside of the product contains pores, and the strength decreases; the PEEK is dried by circulating hot air at 130°C, and the drying time is 4-6H, so that the moisture content in the product is lower than 0.2%. (3) Plasticizing extrusion: through the action of the temperature of the barrel and the screw, the material is transformed into a uniform and continuous melt with a certain fluidity and extruded; the barrel is heated in three zones, and the temperature is set according to the characteristics of the raw material: 1. The temperature of the feeding section in the zone: 355-370°C; the temperature of the melting and compression section in the second zone: 360-380°C; the temperature of the homogenizing section in the third zone: 360-380°C; the joint: 370-390°C; the extrusion screw speed: 8-10r /min. ⑷ Homogenization and diversion: the uniform melt with fluidity enters the main mold through the perforated plate due to the rotary extrusion of the screw, and the melt is further homogenized in the main mold and the melt is changed from spiral motion to linear motion: ① melt Homogenization holding temperature, that is, the set temperature of the main mold: the temperature of the first zone: 330-340℃; the temperature of the first two zones: 330-340℃; the temperature of the latter zone: 330-340℃; . ⑸Forming/Sizing: ①The straight-line flowing melt is evenly flowed into the deflector from the outlet of the main mold, diverted through the V-shaped groove of the deflector, and enters the forming tube of the multi-rod forming mold respectively, and is formed in the forming tube; Flow plate homogenization temperature: 300°C; ② An oil temperature machine is installed at both ends of the shaping box of the forming tube to shape at high temperature to ensure that the product can be extruded smoothly and the surface is smooth; shaping temperature: 150-180°C. ⑹ Traction device: There is a brake seat at the exit of the mold, and the plate product is clamped by adjusting the tightness of the brake bar through the brake seat, so that the molten raw material forms a certain pressure in the compression zone, so that the structure of the extruded product is tight. ⑺Cutting/Stacking: Use a tape measure to measure the length of 1000MM, start the cutting machine, cut out the required length, and stack the bars neatly on a specific stacking rack. There is a stainless square steel between the rod and the rod layer, and the square steel between the layers looks best to be in a straight line up and down. ⑻ Oven heat treatment: When heat treating the stacked PEEK rods, it is mainly divided into sixteen sections:
第一段加温温度40℃ 升温时间20分钟The first heating temperature is 40°C and the heating time is 20 minutes
第二段恒温温度70℃ 恒温时间90分钟The second constant temperature temperature is 70°C and the constant temperature time is 90 minutes
第三段加温温度70℃ 加温时间20分钟The third heating temperature is 70°C and the heating time is 20 minutes
第四段恒温温度100℃ 恒温时间90分钟The fourth section of constant temperature temperature 100 ℃ constant temperature time 90 minutes
第五段加温温度100℃ 加温时间20分钟The fifth heating temperature is 100°C and the heating time is 20 minutes
第六段恒温温度120℃ 恒温时间90分钟The sixth stage constant temperature temperature is 120°C and the constant temperature time is 90 minutes
第七段加温温度120℃ 加温时间20分钟The heating temperature of the seventh stage is 120°C and the heating time is 20 minutes
第八段恒温温度150℃ 恒温时间厚度*2*30分钟The eighth section constant temperature temperature 150 ℃ constant temperature time thickness * 2 * 30 minutes
第九段降温温度150℃ 降温时间20分钟The ninth stage cooling temperature is 150°C and the cooling time is 20 minutes
第十段恒温温度120℃ 恒温时间180分钟The tenth section constant temperature temperature is 120°C and the constant temperature time is 180 minutes
第十一段降温温度120℃ 降温时间20分钟The cooling temperature of the eleventh stage is 120°C and the cooling time is 20 minutes
第十二段恒温温度100℃ 恒温时间180分钟The twelfth section constant temperature temperature 100 ℃ constant temperature time 180 minutes
第十三段降温温度100℃ 降温时间20分钟The thirteenth section cooling temperature 100 ℃ cooling time 20 minutes
第十四段恒温温度70℃ 怛温时间180分钟The fourteenth section constant temperature temperature is 70°C and the temperature time is 180 minutes
第十五段降温温度70℃ 降温时间20分钟The cooling temperature of the fifteenth section is 70°C and the cooling time is 20 minutes
第十六段恒温温度40℃ 温时间180分钟。The sixteenth stage constant temperature temperature is 40°C and the temperature time is 180 minutes.
以上所述仅为本发明的优选实施例,并非因此限制本发明的专利范围,凡是利用本发明说明书及附图内容所作的等效结构或等效流程变换,或直接或间接运用在其他相关的技术领域,均同理包括在本发明的专利保护范围内。The above descriptions are only preferred embodiments of the present invention, and are not intended to limit the patent scope of the present invention. Any equivalent structure or equivalent process transformation made by using the description of the present invention and the contents of the accompanying drawings, or directly or indirectly used in other related All technical fields are equally included in the scope of patent protection of the present invention.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201310738099.0A CN103722718A (en) | 2013-12-25 | 2013-12-25 | PEEK plastic rod production device and process |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201310738099.0A CN103722718A (en) | 2013-12-25 | 2013-12-25 | PEEK plastic rod production device and process |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN103722718A true CN103722718A (en) | 2014-04-16 |
Family
ID=50447135
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201310738099.0A Pending CN103722718A (en) | 2013-12-25 | 2013-12-25 | PEEK plastic rod production device and process |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN103722718A (en) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104015323A (en) * | 2014-05-09 | 2014-09-03 | 东莞市兆科电子材料科技有限公司 | A production method and production line of heat-conducting plastic |
| CN104149312A (en) * | 2014-08-08 | 2014-11-19 | 常州君华特种工程塑料制品有限公司 | Production equipment for continuous extrusion of PEEK sheets and process thereof |
| CN106273352A (en) * | 2016-08-29 | 2017-01-04 | 武汉金牛经济发展有限公司 | The preparation method of a kind of inbred group breeding (PPESK) tubing and device |
| CN106273334A (en) * | 2016-08-31 | 2017-01-04 | 太原理工大学 | A kind of crowded pipe mold for reinforcing glass fiber tubing intensity |
| CN110815769A (en) * | 2019-11-22 | 2020-02-21 | 常州君华医疗科技有限公司 | One-step online crystallization production method of polyether-ether-ketone capillary |
| CN111016111A (en) * | 2019-12-31 | 2020-04-17 | 常州市永邦塑业有限公司 | A kind of PEEK thick-walled pipe extrusion production process and device |
| WO2020125466A1 (en) * | 2018-12-18 | 2020-06-25 | 南京肯特复合材料股份有限公司 | Peek material annealing method |
| CN111844671A (en) * | 2020-07-04 | 2020-10-30 | 东莞市恩欣龙特种材料有限公司 | Special process method for producing PBT plastic rod |
| CN115027079A (en) * | 2022-06-27 | 2022-09-09 | 江苏君华特种工程塑料制品有限公司 | Method for reducing thickness of oxide layer by removing stress of special engineering plastic profile |
| CN117484819A (en) * | 2023-12-19 | 2024-02-02 | 广州宇工新材料科技有限公司 | A method for preparing glass fiber reinforced PEEK composite parts |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20030086331A1 (en) * | 2001-11-08 | 2003-05-08 | Jun-Rong Lin | Extrusion molding machine |
| CN103101167A (en) * | 2012-12-20 | 2013-05-15 | 刘福华 | PP (propene polymer) raw material rod production process |
| CN103101168A (en) * | 2012-12-20 | 2013-05-15 | 刘福华 | POM(polyformaldehyde) raw material rod production process |
-
2013
- 2013-12-25 CN CN201310738099.0A patent/CN103722718A/en active Pending
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20030086331A1 (en) * | 2001-11-08 | 2003-05-08 | Jun-Rong Lin | Extrusion molding machine |
| CN103101167A (en) * | 2012-12-20 | 2013-05-15 | 刘福华 | PP (propene polymer) raw material rod production process |
| CN103101168A (en) * | 2012-12-20 | 2013-05-15 | 刘福华 | POM(polyformaldehyde) raw material rod production process |
Non-Patent Citations (2)
| Title |
|---|
| 刘西文等: "《塑料挤出工(中、高级)培训教程》", 31 January 2013, 印刷工业出版社 * |
| 张甲敏: "《塑料技术及典型工艺实例》", 31 July 2010, 化学工业出版社 * |
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104015323A (en) * | 2014-05-09 | 2014-09-03 | 东莞市兆科电子材料科技有限公司 | A production method and production line of heat-conducting plastic |
| CN104149312A (en) * | 2014-08-08 | 2014-11-19 | 常州君华特种工程塑料制品有限公司 | Production equipment for continuous extrusion of PEEK sheets and process thereof |
| CN106273352A (en) * | 2016-08-29 | 2017-01-04 | 武汉金牛经济发展有限公司 | The preparation method of a kind of inbred group breeding (PPESK) tubing and device |
| CN106273334A (en) * | 2016-08-31 | 2017-01-04 | 太原理工大学 | A kind of crowded pipe mold for reinforcing glass fiber tubing intensity |
| WO2020125466A1 (en) * | 2018-12-18 | 2020-06-25 | 南京肯特复合材料股份有限公司 | Peek material annealing method |
| CN110815769A (en) * | 2019-11-22 | 2020-02-21 | 常州君华医疗科技有限公司 | One-step online crystallization production method of polyether-ether-ketone capillary |
| CN111016111A (en) * | 2019-12-31 | 2020-04-17 | 常州市永邦塑业有限公司 | A kind of PEEK thick-walled pipe extrusion production process and device |
| CN111844671A (en) * | 2020-07-04 | 2020-10-30 | 东莞市恩欣龙特种材料有限公司 | Special process method for producing PBT plastic rod |
| CN115027079A (en) * | 2022-06-27 | 2022-09-09 | 江苏君华特种工程塑料制品有限公司 | Method for reducing thickness of oxide layer by removing stress of special engineering plastic profile |
| CN115027079B (en) * | 2022-06-27 | 2023-09-05 | 江苏君华特种工程塑料制品有限公司 | Method for reducing thickness of oxide layer by destressing special engineering plastic profile |
| CN117484819A (en) * | 2023-12-19 | 2024-02-02 | 广州宇工新材料科技有限公司 | A method for preparing glass fiber reinforced PEEK composite parts |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103722717B (en) | A kind of PEI sticking plaster production equipment and process | |
| CN102490380B (en) | Packing belt production method and complete equipment | |
| CN104629254B (en) | A kind of manufacture method of continuous lod polyether-ether-ketone composite material prepreg tape and equipment | |
| CN109080102B (en) | Wire drawing process of plastic woven bag | |
| CN102501359B (en) | POM plate extrusion molding method | |
| CN103753796A (en) | Equipment and process for production of PPS plastic board | |
| CN103101165B (en) | A kind of method and device producing PA material plate | |
| CN104760250A (en) | PPS plastic rod production device and production method | |
| CN103101164A (en) | Production process and device of PC (poly carbonate) raw material sheet material | |
| CN103101163A (en) | Production process and device of ABS (acrylonitrile butadiene styreneacrylonitrile butadiene styrene) raw material sheet material | |
| CN106273303A (en) | The preparation method of a kind of inbred group breeding (PPESK) tubing and device | |
| CN205148865U (en) | A double screw extruder for production of polyethylene foam sheet | |
| CN107186993A (en) | A kind of tube forming equipment extrusion die | |
| CN211941969U (en) | Die head hoisting device in sheet extrusion molding machine | |
| CN204054566U (en) | Single screw extruder | |
| CN102267224A (en) | Quick-cooling heated mold injection molding process and equipment thereof | |
| CN2749665Y (en) | Core internal cooling extrusion dies | |
| CN103101168A (en) | POM(polyformaldehyde) raw material rod production process | |
| CN208068836U (en) | Polyethylene pipe extrusion device | |
| CN203393282U (en) | Device for producing ribbon-like filaments by utilizing waste PET (Polyethylene Glycol Terephthalate) | |
| CN203919802U (en) | The quick extruder of a kind of carbon-point | |
| CN212021599U (en) | Degradable sheet extrusion moulding machine | |
| CN204773484U (en) | Horizontal single screw rod plastics extruder device | |
| CN203901777U (en) | Multi-outlet rapid carbon rod extruder | |
| CN204471842U (en) | A kind of constant temperature plastic extruder |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20140416 |
|
| RJ01 | Rejection of invention patent application after publication |