CN103406601A - Vertical-type five-shaft linkage gear hobbing machine tool - Google Patents
Vertical-type five-shaft linkage gear hobbing machine tool Download PDFInfo
- Publication number
- CN103406601A CN103406601A CN2013102990694A CN201310299069A CN103406601A CN 103406601 A CN103406601 A CN 103406601A CN 2013102990694 A CN2013102990694 A CN 2013102990694A CN 201310299069 A CN201310299069 A CN 201310299069A CN 103406601 A CN103406601 A CN 103406601A
- Authority
- CN
- China
- Prior art keywords
- hob
- axis
- frame
- servo motor
- vertical
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Landscapes
- Gear Processing (AREA)
Abstract
本发明提供了一种立式五轴联动滚齿加工机床,包括机架,滚刀架通过立柱设于机架上,滚刀架上设有滚刀,第一伺服电机连接滚刀,第二伺服电机连接立柱;工作台通过托架设于机架上,用于驱动待加工工件齿坯绕自轴旋转的第三伺服电机设于工作台上,第四伺服电机连接工作台,第五伺服电机连接托架;待加工工件齿坯轴线与工作台水平面垂直。本发明提供的装置克服了现有技术的不足,能高效率、高精度地加工非圆齿轮,对中等大小型、小型非圆齿轮或斜齿非圆齿轮滚齿的加工均适用。
The invention provides a vertical five-axis linkage gear hobbing machine tool, which includes a frame, a hob frame is set on the frame through a column, a hob is arranged on the hob frame, a first servo motor is connected to the hob, and a second servo motor is connected to the hob. The servo motor is connected to the column; the workbench is set on the frame through the bracket, and the third servo motor for driving the tooth blank of the workpiece to be processed to rotate around its own axis is set on the workbench, the fourth servo motor is connected to the workbench, and the fifth servo The motor is connected to the bracket; the axis of the tooth blank of the workpiece to be processed is perpendicular to the horizontal plane of the worktable. The device provided by the invention overcomes the shortcomings of the prior art, can process non-circular gears with high efficiency and high precision, and is suitable for hobbing medium-sized and small non-circular gears or helical non-circular gears.
Description
技术领域technical field
本发明涉及一种立式五轴联动滚齿加工机床,属于滚齿加工机床技术领域。The invention relates to a vertical five-axis linkage hobbing machine tool, which belongs to the technical field of gear hobbing machine tools.
背景技术Background technique
公知,目前国内还未有真正专业高效生产非圆齿轮的数控滚齿加工机床,现在对非圆齿轮的加工一般多采用线切割或数控插齿机床加工,对于精度不高的非圆齿轮还可通过近似铣齿的方法来加工得到,但这些加工方法效率均不高,精度也有限,而且不能加工斜齿非圆齿轮。随着现代机械行业对传动平稳性、低噪声等方面要求的提高以及快速设计等方面的考虑,斜齿非圆齿轮在这些方面的优势正越来越受到国内外学者的关注和重视,其应用也越来越广泛,因此,对能大量生产斜齿非圆齿轮的加工机床也提出了迫切需求。As we all know, there is no CNC gear hobbing machine tool that can produce non-circular gears professionally and efficiently in China at present. Wire cutting or CNC gear shaping machine tools are generally used for the processing of non-circular gears, and non-circular gears with low precision can also be processed. It is processed by approximate milling methods, but these processing methods are not efficient, the accuracy is limited, and they cannot process helical non-circular gears. With the improvement of the modern machinery industry's requirements for transmission stability, low noise, etc., and the consideration of rapid design, the advantages of helical non-circular gears in these aspects are attracting more and more attention and attention from scholars at home and abroad. It is also becoming more and more widespread, so there is an urgent demand for processing machine tools that can mass produce helical and non-circular gears.
现有的斜齿非圆齿轮滚齿加工方法主要有四轴联动滚齿加工方法和五轴联动滚齿加工方法,其中四轴联动滚齿加工方法由于其加工过程中滚刀切削变化大,加工同样的斜齿非圆齿轮比五轴联动需要更长的滚刀长度和轴向更大的进刀位移,因此适合于加工小型的斜齿非圆齿轮。五轴联动加工不受四轴联动滚齿加工滚刀长度、切削量变化大、更大轴向进刀位移等限制,因此其对加工大型斜齿非圆齿轮特别适合。The existing hobbing methods for helical non-circular gears mainly include four-axis simultaneous hobbing processing methods and five-axis simultaneous gear hobbing processing methods. The same helical non-circular gear requires a longer hob length and a larger axial feed displacement than the five-axis linkage, so it is suitable for processing small helical non-circular gears. Five-axis simultaneous machining is not limited by the length of the four-axis simultaneous gear hobbing hob, the large change in cutting amount, and the larger axial feed displacement, so it is especially suitable for processing large helical non-circular gears.
滚齿机床按其结构布置可分为卧式和立式两大类,一般而言,立式滚齿机由于工件重力方向即为支撑的机座,因此其受力好适合于加工大型和重型齿轮的滚齿加工;卧式滚齿机主要靠轴的的径向受力来支撑齿坯的重量,由于工件大时,轴受力大,轴向易变形,因此不适应加工大型齿轮,但其结构灵活轻便,响应快,价格低廉因此特别适合于小型齿轮的加工。Gear hobbing machine tools can be divided into two categories: horizontal and vertical according to their structural layout. Generally speaking, because the direction of gravity of the workpiece is the supporting frame of the vertical gear hobbing machine, its force is good and it is suitable for processing large and heavy gears. Gear processing; the horizontal gear hobbing machine mainly relies on the radial force of the shaft to support the weight of the gear blank. When the workpiece is large, the force on the shaft is large and the axial direction is easy to deform, so it is not suitable for processing large gears, but its structure is flexible and light. The response is fast and the price is low, so it is especially suitable for the processing of small gears.
发明内容Contents of the invention
本发明要解决的技术问题是提供一种能高效率、高精度地加工非圆齿轮的立式五轴联动滚齿加工机床。The technical problem to be solved by the present invention is to provide a vertical five-axis gear hobbing machine tool capable of processing non-circular gears with high efficiency and high precision.
为了解决上述技术问题,本发明的技术方案是提供一种立式五轴联动滚齿加工机床,其特征在于:包括机架,滚刀架通过立柱设于机架上,滚刀架上设有滚刀,第一伺服电机连接滚刀,第二伺服电机连接立柱;工作台通过托架设于机架上,用于驱动待加工工件齿坯绕自轴旋转的第三伺服电机设于工作台上,第四伺服电机连接工作台,第五伺服电机连接托架;待加工工件齿坯轴线与工作台水平面垂直。In order to solve the above technical problems, the technical solution of the present invention is to provide a vertical five-axis linkage hobbing machine tool, which is characterized in that: it includes a frame, the hob frame is set on the frame through a column, and the hob frame is equipped with Hob, the first servo motor is connected to the hob, the second servo motor is connected to the column; the workbench is set on the frame through the bracket, and the third servomotor for driving the tooth blank of the workpiece to be processed to rotate around its own axis is set on the workbench Above, the fourth servo motor is connected to the workbench, and the fifth servo motor is connected to the bracket; the axis of the tooth blank of the workpiece to be processed is perpendicular to the horizontal plane of the workbench.
优选地,所述第二伺服电机与立柱之间通过滚珠丝杆连接。Preferably, the second servo motor is connected to the column through a ball screw.
优选地,所述第四伺服电机与工作台之间通过滚珠丝杆连接。Preferably, the fourth servo motor is connected to the worktable through a ball screw.
优选地,所述第五伺服电机与托架之间通过滚珠丝杆连接。Preferably, the fifth servo motor is connected to the bracket through a ball screw.
本发明提供的一种立式五轴联动滚齿加工机床工作时,第一伺服电机驱动滚刀绕自轴旋转;第二伺服电机带动滚珠丝杆驱动立柱,立柱的运动带动滚刀架运动使滚刀沿齿坯轴向进刀;第三伺服电机驱动齿坯绕自轴旋转;第四伺服电机驱动工作台,使工作台上安装的齿坯沿其中心与滚刀中心变化;第五伺服电机驱动滚珠丝杆,滚珠丝杆上移动螺母与托架连接成一个整体,从而带动托架运动,工作台沿齿坯切向运动。When the vertical five-axis linkage hobbing machine tool provided by the present invention is working, the first servo motor drives the hob to rotate around its own axis; the second servo motor drives the ball screw to drive the column, and the movement of the column drives the hob frame to move The hob feeds along the axial direction of the gear blank; the third servo motor drives the gear blank to rotate around its own axis; the fourth servo motor drives the worktable so that the gear blank installed on the worktable changes along its center and the center of the hob; the fifth servo The motor drives the ball screw, and the moving nut on the ball screw is connected with the bracket as a whole, thus driving the bracket to move, and the worktable moves tangentially along the gear blank.
本发明提供的装置克服了现有技术的不足,能高效率、高精度地加工非圆齿轮,对中等大小型、小型非圆齿轮或斜齿非圆齿轮滚齿的加工均适用。The device provided by the invention overcomes the shortcomings of the prior art, can process non-circular gears with high efficiency and high precision, and is suitable for hobbing medium-sized and small non-circular gears or helical non-circular gears.
附图说明Description of drawings
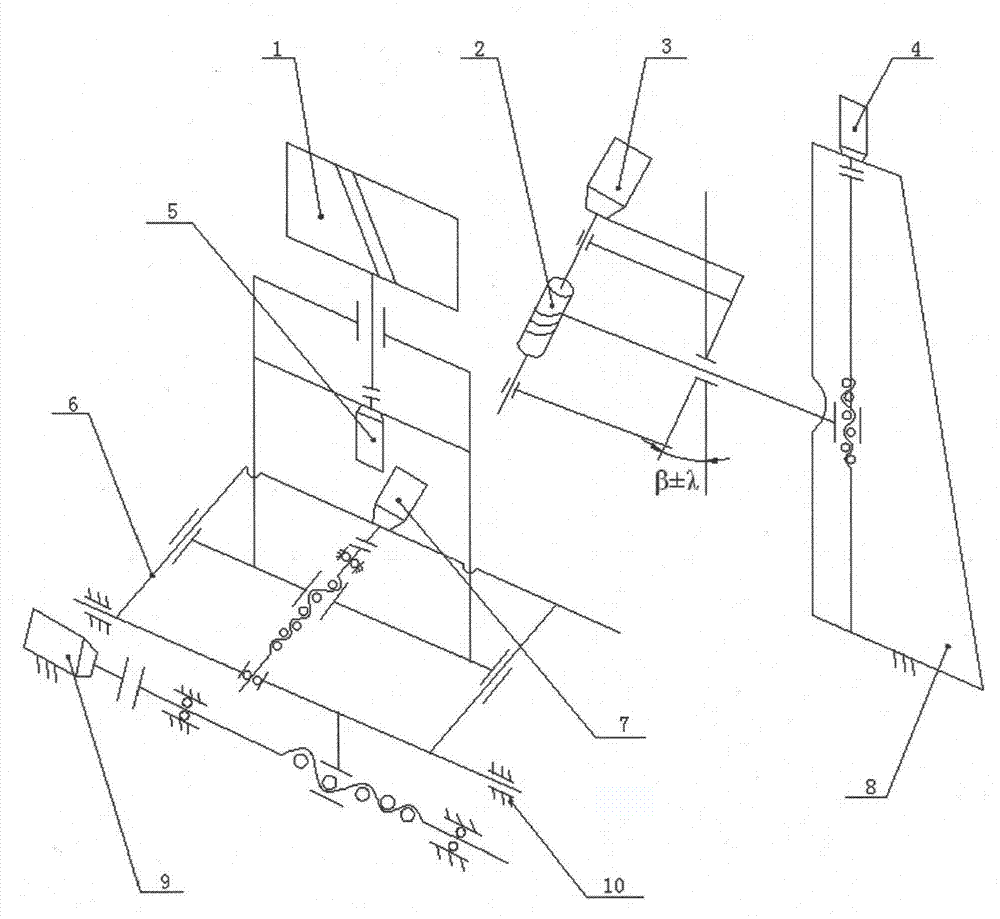
图1为本发明提供的立式五轴联动滚齿加工机床示意图;Fig. 1 is a schematic diagram of a vertical five-axis gear hobbing machine tool provided by the present invention;
图2为本发明提供的立式五轴联动滚齿加工机床适应凸节曲线斜齿非圆齿轮数控滚齿加工的数控系统原理图。Fig. 2 is a schematic diagram of the numerical control system of the vertical five-axis linkage hobbing machine tool provided by the present invention, which is suitable for the numerical control hobbing of convex curve helical non-circular gears.
具体实施方式Detailed ways
为使本发明更明显易懂,兹以一优选实施例,并配合附图作详细说明如下。In order to make the present invention more comprehensible, a preferred embodiment is described in detail below with accompanying drawings.
图1为本发明提供的立式五轴联动滚齿加工机床示意图,所述的立式五轴联动滚齿加工机床包括机架10,滚刀架通过立柱8安装在机架10上,滚刀架与立柱8为固定连接,滚刀架上装有滚刀2,第一伺服电机3连接滚刀2,第二伺服电机4连接立柱8,整个立柱部分均布置在机架10一侧;托架6安装在机架10上另一侧,工作台安装在托架6上,用于驱动待加工工件齿坯1绕自轴旋转的第三伺服电机5装在工作台上,第四伺服电机7连接工作台,第五伺服电机9连接托架6。角度β±λ为滚刀2安装角,需根据实际加工方法确定具体“+”或“-”符号。Figure 1 is a schematic diagram of a vertical five-axis gear hobbing machine tool provided by the present invention. The vertical five-axis gear hobbing machine tool includes a
齿坯1安装在工作台上,齿坯1的安装为立式安装方式,即齿坯1轴线与工作台水平面垂直。The tooth blank 1 is installed on the worktable, and the installation of the tooth blank 1 is a vertical installation, that is, the axis of the tooth blank 1 is perpendicular to the horizontal plane of the worktable.
第一伺服电机3驱动滚刀2绕自轴旋转;第二伺服电机4带动滚珠丝杆驱动立柱8,立柱8的运动带动滚刀架运动使滚刀2沿齿坯1轴向进刀;第三伺服电机5驱动齿坯1绕自轴旋转;第四伺服电机7驱动工作台,使工作台上安装的齿坯1沿其中心与滚刀2中心变化;第五伺服电机9驱动滚珠丝杆,滚珠丝杆上移动螺母与托架6连接成一个整体,从而带动托架6运动,工作台沿齿坯1切向运动。The
滚刀2绕自轴的旋转和齿坯1绕自轴的旋转均直接由伺服电机或电主轴驱动,立柱8、工作台及托架6的运动均由伺服电机带动滚珠丝杆驱动。The rotation of the hob 2 around its own axis and the rotation of the gear blank 1 around its own axis are directly driven by a servo motor or an electric spindle, and the movement of the
图2所示为本发明适应凸节曲线斜齿非圆齿轮数控滚齿加工的数控系统原理图,O0、X0、Y0、Z0构成原始三维坐标,O1、X1、Y1、Z1构成运动后三维坐标。系统由工作台、滚刀架、滚刀、机架等部件组成,包括齿轮坯绕Z1轴的回转运动A、滚刀绕自轴的旋转运动B、工作台在非圆齿轮坯转动时沿Y0向的相对平移运动C、滚刀架在齿轮坯转动时沿X0向的相对平移运动D、滚刀架沿齿轮坯轴向进给运动E。上述五个自由度运动在加工过程中形成严格的联动关系,即各运动之间必须按照给定的规律做恒速与变速运动,其中滚刀沿齿坯轴向进刀时齿轮坯的回转运动A、B包含由滚刀架沿齿轮坯轴向进给运动D引起的附加运动。Fig. 2 is a schematic diagram of the numerical control system adapted to the numerical control hobbing of convex curve helical non-circular gears according to the present invention, O 0 , X 0 , Y 0 , Z 0 constitute the original three-dimensional coordinates, O 1 , X 1 , Y 1 , Z 1 constitute the three-dimensional coordinates after movement. The system is composed of workbench, hob frame, hob, frame and other components, including the rotary motion A of the gear blank around the Z 1 axis, the rotary motion B of the hob around its own axis, and the working table along the The relative translational movement C in the Y 0 direction, the relative translational movement D of the hob along the X 0 direction when the gear blank rotates, and the feed movement E of the hob along the axial direction of the gear blank. The above-mentioned five degrees of freedom movements form a strict linkage relationship in the process of processing, that is, each movement must perform constant speed and variable speed movement according to a given rule, and the rotary motion of the gear blank when the hob feeds along the axial direction A and B contain the additional motion caused by the axial feed motion D of the hob along the gear blank.
本发明提供的立式五轴联动滚齿加工机床主要针对加工非圆齿轮,尤其是斜齿非圆齿轮,适用于加工中等大小(最大极径100~600mm)的非圆齿轮,尤其适用于五轴联动滚齿加工非圆齿轮方法;对于小型(最大极径100mm以下)的斜齿非圆齿轮也可采用五轴或四轴联动滚齿方法在此机床上进行滚齿加工。The vertical five-axis linkage hobbing machine tool provided by the present invention is mainly aimed at processing non-circular gears, especially helical non-circular gears, and is suitable for processing non-circular gears of medium size (maximum pole diameter 100-600mm), especially suitable for five Axis linkage hobbing method for non-circular gears; for small (maximum pole diameter below 100mm) helical non-circular gears, five-axis or four-axis linkage hobbing method can also be used for hobbing on this machine tool.
当加工中等大小非圆齿轮或斜齿非圆齿轮时,在机床上采用五轴联动滚齿加工法加工,具体过程可分为两步:When machining medium-sized non-circular gears or helical non-circular gears, the five-axis hobbing method is used on the machine tool. The specific process can be divided into two steps:
1)滚刀没有沿齿坯轴向方向的进刀,即滚刀沿齿坯圆周滚切加工时,四轴联动,即:滚刀绕自轴运动、齿坯绕自轴运动、滚刀与齿坯中心距位移变化,滚刀沿齿坯圆周切向的运动,这种切削运动是最主要的切削运动;1) The hob does not feed along the axial direction of the gear blank, that is, when the hob hobs along the circumference of the gear blank, the four-axis linkage, that is: the hob moves around its own axis, the gear blank moves around its own axis, the hob and The displacement of the center distance of the tooth blank changes, and the hob moves tangentially along the circumference of the tooth blank. This cutting movement is the most important cutting movement;
2)当滚刀有沿齿坯轴向进刀的时,运动状态变为五轴联动,即:滚刀沿齿坯轴向方向的运动、滚刀绕自轴运动、齿坯绕自轴运动、滚刀与齿坯中心距位移变化、滚刀沿齿坯圆周切向的运动,因为轴向进刀只在滚刀沿齿坯圆周切削完毕后才进行,因此这种滚齿切削运动不是最主要的切削运动。2) When the hob feeds along the axial direction of the gear blank, the motion state becomes five-axis linkage, that is: the movement of the hob along the axial direction of the gear blank, the movement of the hob around its own axis, and the movement of the gear blank around its own axis , The displacement change of the center distance between the hob and the gear blank, and the tangential movement of the hob along the circumference of the gear blank, because the axial feed is only carried out after the hob completes cutting along the circumference of the gear blank, so this hobbing cutting movement is not the most optimal Primary cutting motion.
当加工小型非圆齿轮或斜齿非圆齿轮时,这时也可采用四轴联动方式滚齿加工,其具体过程又分为两步:When processing small non-circular gears or helical non-circular gears, four-axis linkage hobbing can also be used at this time, and the specific process is divided into two steps:
1)滚刀没有沿齿坯轴向方向的进刀,即滚刀沿齿坯圆周滚切加工时,三轴联动滚齿,即:滚刀绕自轴运动、齿坯绕自轴运动、滚刀与齿坯中心距位移变化,这种切削运动是最主要的切削运动;1) The hob does not feed along the axial direction of the gear blank, that is, when the hob is hobbing along the circumference of the gear blank, the gear hobbing is performed in three-axis linkage, that is: the hob moves around its own axis, the gear blank moves around its own axis, hobbing The displacement of the center distance between the knife and the gear blank changes, and this cutting motion is the most important cutting motion;
2)当滚刀有沿齿坯轴向进刀时,这时的运动状态加上滚刀绕自轴运动、齿坯绕自轴运动、滚刀与齿坯中心距位移变化联动变为四轴联动,这种滚齿切削运动不是最主要的切削运动。2) When the hob feeds along the axial direction of the gear blank, the motion state at this time plus the movement of the hob around its own axis, the movement of the gear blank around its own axis, and the linkage between the displacement change of the center distance between the hob and the gear blank become four-axis Linkage, this hobbing cutting motion is not the most important cutting motion.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2013102990694A CN103406601A (en) | 2013-07-16 | 2013-07-16 | Vertical-type five-shaft linkage gear hobbing machine tool |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2013102990694A CN103406601A (en) | 2013-07-16 | 2013-07-16 | Vertical-type five-shaft linkage gear hobbing machine tool |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN103406601A true CN103406601A (en) | 2013-11-27 |
Family
ID=49599668
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2013102990694A Pending CN103406601A (en) | 2013-07-16 | 2013-07-16 | Vertical-type five-shaft linkage gear hobbing machine tool |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN103406601A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105665838A (en) * | 2016-03-24 | 2016-06-15 | 厦门理工学院 | Machining method for cycloid gear |
| CN109514009A (en) * | 2018-12-25 | 2019-03-26 | 江西福格新能源传动技术有限公司 | Helical gears gear hobbing roll flute is integrally machined equipment |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS597519A (en) * | 1982-07-02 | 1984-01-14 | Nissan Motor Co Ltd | Cutting method of gear |
| CN101244474A (en) * | 2008-03-25 | 2008-08-20 | 东华大学 | A CNC hobbing method for helical elliptical gears and helical non-circular gears |
| CN101829814A (en) * | 2010-03-15 | 2010-09-15 | 岑益南 | Hard-surface gear hobbing processing device |
| CN202591751U (en) * | 2012-04-01 | 2012-12-12 | 李文辉 | Numerical-control gear hobbing machine |
| CN203380437U (en) * | 2013-07-16 | 2014-01-08 | 东华大学 | Vertical five-axis linkage gear hobbing machine tool |
-
2013
- 2013-07-16 CN CN2013102990694A patent/CN103406601A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS597519A (en) * | 1982-07-02 | 1984-01-14 | Nissan Motor Co Ltd | Cutting method of gear |
| CN101244474A (en) * | 2008-03-25 | 2008-08-20 | 东华大学 | A CNC hobbing method for helical elliptical gears and helical non-circular gears |
| CN101829814A (en) * | 2010-03-15 | 2010-09-15 | 岑益南 | Hard-surface gear hobbing processing device |
| CN202591751U (en) * | 2012-04-01 | 2012-12-12 | 李文辉 | Numerical-control gear hobbing machine |
| CN203380437U (en) * | 2013-07-16 | 2014-01-08 | 东华大学 | Vertical five-axis linkage gear hobbing machine tool |
Non-Patent Citations (1)
| Title |
|---|
| 史勇: "非圆齿轮加工法研究及斜齿非圆齿轮滚齿加工过程仿真", 《中国优秀硕士学位论文全文数据库 工程科技Ⅰ辑》, no. 6, 15 June 2013 (2013-06-15) * |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105665838A (en) * | 2016-03-24 | 2016-06-15 | 厦门理工学院 | Machining method for cycloid gear |
| CN105665838B (en) * | 2016-03-24 | 2019-01-01 | 厦门理工学院 | A kind of processing method of cycloid gear |
| CN109514009A (en) * | 2018-12-25 | 2019-03-26 | 江西福格新能源传动技术有限公司 | Helical gears gear hobbing roll flute is integrally machined equipment |
| CN109514009B (en) * | 2018-12-25 | 2024-05-17 | 江西福格新能源传动技术有限公司 | Helical gear hobbing and grinding integrated processing equipment |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102151909B (en) | Large-scale numerical control gear machining machine tool | |
| CN202037476U (en) | Large-scale numerical control gear cutting machine | |
| CN202411844U (en) | Rotary table mechanism for combined boring and milling machine tool of gantry drill | |
| CN203109692U (en) | Vertical-type numerically-controlled machine tool main shaft swinging device | |
| CN201711768U (en) | Pentahedral milling head for numerically-controlled gantry machining center | |
| CN201427188Y (en) | Square machine tool of multifunctional numerical control lathe | |
| CN201300235Y (en) | Numerical-control double-spindle milling machine for the star-wheel sheet processing | |
| CN104924181B (en) | A kind of utilization circular cylindrical coordinate three-shaft linkage lathe realizes the method and apparatus with the full profile grinding of tenon blade | |
| CN205008689U (en) | Horizontal skewed tooth non -circular gear gear hobbing processing lathe of five -axle linkage | |
| CN103143789A (en) | Gear cutting machine | |
| CN201833178U (en) | Numerical control turning and boring machine tool | |
| CN204893101U (en) | Tooth machine is milled in numerical control | |
| CN103111646A (en) | Composite numerical controlled lathe and power cutter tower thereof | |
| CN103273425A (en) | CBN grinding wheel track finishing device | |
| CN101979202B (en) | Face gear numerical control machining device and machining method | |
| CN204843183U (en) | Complicated curved surface wire -electrode cutting diaxon numerical control revolving platform | |
| CN2649242Y (en) | Numerically controlled spiral bevel gear milling machine layout | |
| CN101513726A (en) | Follow-up grinding method and digital controller thereof | |
| CN104441080A (en) | Double-swing five-shaft head | |
| CN201271802Y (en) | Major diameter wheel flange teeth groove processing system | |
| CN109746529A (en) | A large-scale zero-degree spiral bevel gear forming and milling processing method and processing device | |
| CN201267903Y (en) | Ring surface worm screw numerically controlled machine of virtual rotation center | |
| CN201702463U (en) | Straight bevel gear machine tool | |
| CN203380437U (en) | Vertical five-axis linkage gear hobbing machine tool | |
| CN201881011U (en) | Numerical-controlled worm gear machining device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20131127 |