CN103008480A - High-precision blanking die structure of steel battery shell - Google Patents
High-precision blanking die structure of steel battery shell Download PDFInfo
- Publication number
- CN103008480A CN103008480A CN2012105330225A CN201210533022A CN103008480A CN 103008480 A CN103008480 A CN 103008480A CN 2012105330225 A CN2012105330225 A CN 2012105330225A CN 201210533022 A CN201210533022 A CN 201210533022A CN 103008480 A CN103008480 A CN 103008480A
- Authority
- CN
- China
- Prior art keywords
- blanking
- die
- plate
- mold
- upper die
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Landscapes
- Sealing Battery Cases Or Jackets (AREA)
Abstract
本发明公开了一种电池钢壳高精度落料模具结构,应用于薄壁电池钢壳的生产技术中,其包括上模架板和冲床工作台板,所述上模架板的下方安装有落料上模板和拉伸上模固定板,所述落料上模板上安装落料上模,所述拉伸上模固定板上设置有多个平行间隔布置的拉伸冲头,所述冲床工作台板上对应落料上模板、拉伸冲头设置有落料下模板和拉伸凹模,所述落料下模板上安装落料下模,所述上模架板与冲床工作台板之间安装由模架导套和模架导柱组成的导向机构,所述落料上、下模板之间设置有独立的定位导向组件。上述模具结构不仅提高了上下模的配合精度,延长了模具寿命;而且拆装方便,缩短了维修时间,提高了生产效率。
The invention discloses a high-precision blanking mold structure for battery steel shells, which is applied in the production technology of thin-walled battery steel shells. It includes an upper mold frame plate and a punch worktable. A blanking upper die and a stretching upper die fixing plate, a blanking upper die is installed on the blanking upper die, a plurality of stretching punches arranged in parallel at intervals are arranged on the drawing upper die fixing plate, the punching machine The blanking lower template and the drawing die are provided on the working table corresponding to the blanking upper template and the stretching punch. A guide mechanism composed of formwork guide sleeves and formwork guide columns is installed between them, and an independent positioning guide assembly is arranged between the blanking upper and lower formworks. The above mold structure not only improves the matching precision of the upper and lower molds and prolongs the life of the mold, but also facilitates disassembly and assembly, shortens maintenance time and improves production efficiency.
Description
技术领域 technical field
本发明涉及一种薄壁电池壳生产模具,尤其是涉及一种电池钢壳高精度落料模具结构。The invention relates to a production mold for a thin-walled battery case, in particular to a high-precision blanking mold structure for a battery steel case.
背景技术 Background technique
目前,薄壁电池钢壳一般都采用级进模冲制。请参阅图1所示,图1是传统的电池钢壳落料模具结构的示意图,其包括上模架板10和对应设置于上模架板10下方的冲床工作台板11,所述上模架板10的下方安装有落料上模板12和拉伸上模固定板13,所述落料上模板12上安装落料上模,所述拉伸上模固定板13上依次设置有多个平行间隔布置的拉伸冲头14,所述冲床工作台板11上对应落料上模板12、拉伸冲头14设置有落料下模板15和拉伸凹模16,所述落料下模板15上安装落料下模,所述上模架板10与冲床工作台板11之间安装由模架导套17和模架导柱18组成的导向机构。这种模具结构的特点是,整个7~10道上模:包括落料上模及拉伸冲头14全部集成在一块上模架板上,而下模部分则是单道独立紧固在工作台板上。整套模具往往只采用一套(两副)模架导套17和模架导柱18来保证上下模的位置度,即整个上模架板10与下面冲床工作台板11之间,共用一套导柱导套。这种结构的模具,从理论上及使用效果来看,也是可行的,而且在行业中已流行了多年。At present, thin-walled battery steel cases are generally punched by progressive dies. Please refer to Fig. 1, Fig. 1 is a schematic diagram of a traditional battery steel shell blanking mold structure, which includes an upper
但是也存在一定的缺陷。因为这种模具结构作为拉伸部分来说,所有拉伸冲头14全部安装在一整块拉伸上模固定板13上,拉伸冲头14相互之间固然不会产生位移,然而落料模是单独紧固在上模架板10上的,在运行中,难免不与上模架板10产生位移。整个上模架板10及拉伸上模固定板13依靠导柱导套,保证了与下模的配合,却不一定能保证落料模上下的位置度(况且落料下模也是独立紧固在工作台板上的)。这样,有时偏差大了,落料模就会出现崩刃现象。另外,落料模相对于拉伸模来讲,维修的次数要多得多(因为要经常修磨刃口),由于没有定位保证,每次拆装都要多次调校上下模位置,所以比较费事麻烦。But there are also certain defects. Because this kind of die structure is taken as the stretching part, all the
发明内容 Contents of the invention
本发明的目的在于提供一种电池钢壳高精度落料模具结构,其具有上下模配合精度高、拆装便捷以及模具使用寿命长的特点,以解决现有技术中电池钢壳高精度落料模具结构存在的问题。The purpose of the present invention is to provide a high-precision blanking mold structure for battery steel shells, which has the characteristics of high matching precision between the upper and lower molds, convenient disassembly and assembly, and long service life of the mold, so as to solve the problem of high-precision blanking of battery steel shells in the prior art. There are problems with the mold structure.
本发明的目的是通过以下技术方案来实现:The purpose of the present invention is to realize through the following technical solutions:
一种电池钢壳高精度落料模具结构,其包括上模架板和对应设置于上模架板下方的冲床工作台板,所述上模架板的下方安装有落料上模板和拉伸上模固定板,所述落料上模板上安装落料上模,所述拉伸上模固定板上设置有多个平行间隔布置的拉伸冲头,所述冲床工作台板上对应落料上模板、拉伸冲头设置有落料下模板和拉伸凹模,所述落料下模板上安装落料下模,所述上模架板与冲床工作台板之间安装由模架导套和模架导柱组成的导向机构,其中,所述落料上、下模板之间设置有独立的定位导向组件。A high-precision blanking mold structure for battery steel shells, which includes an upper mold frame plate and a punching workbench correspondingly arranged below the upper mold frame plate, and a blanking upper template and a stretching plate are installed below the upper mold frame plate. The upper die fixing plate, the blanking upper die is installed on the blanking upper die, the drawing upper die fixing plate is provided with a plurality of stretching punches arranged in parallel at intervals, and the corresponding blanking on the punching table is The upper template and the stretching punch are provided with a blanking lower template and a drawing die, the blanking lower mold is installed on the blanking lower template, and the mold frame guide A guide mechanism composed of a sleeve and a formwork guide post, wherein an independent positioning guide assembly is arranged between the blanking upper and lower templates.
特别地,所述定位导向组件包括安装于落料上模板上的落料模导套和安装于落料下模板上的落料模导柱。In particular, the positioning guide assembly includes a blanking die guide sleeve installed on the blanking upper formwork and a blanking die guide post installed on the blanking lower formwork.
特别地,所述落料模导套和落料模导柱设置为两副。In particular, the blanking die guide sleeve and the blanking die guide post are provided in two sets.
特别地,所述落料模导柱、套与模架导柱、套之间呈纵横两个方向排列。In particular, the guide pillars and sleeves of the blanking die are arranged vertically and horizontally with the guide pillars and sleeves of the formwork.
本发明的有益效果为,所述电池钢壳高精度落料模具结构与现有技术相比于落料模的上下模板上再加了一套(两副)导柱导套,使之有了独立的定位系统。另外,落料模导柱导套与模架导柱导套现在成纵横两个方向排列,更加提高了上下模的配合精度。这样,不但避免了模具崩刃现象,延长了模具寿命;而且在拆装模具时,只要安装就位就行,不必多次调校上下模位置,简化了安装手续,缩短了维修时间,提高了生产效率。The beneficial effect of the present invention is that, compared with the prior art, the structure of the high-precision blanking mold for the battery steel shell is equipped with a set (two pairs) of guide posts and guide sleeves on the upper and lower templates of the blanking mold, so that it has Independent positioning system. In addition, the blanking die guide post guide sleeve and the mold base guide post guide sleeve are now arranged in vertical and horizontal directions, which further improves the matching accuracy of the upper and lower dies. In this way, it not only avoids the phenomenon of mold chipping, but also prolongs the life of the mold; and when disassembling the mold, as long as it is installed in place, it is not necessary to adjust the position of the upper and lower molds many times, which simplifies the installation procedure, shortens the maintenance time, and improves the production. efficiency.
附图说明 Description of drawings
图1是传统的电池钢壳落料模具结构的示意图;Fig. 1 is the schematic diagram of traditional battery steel case blanking mold structure;
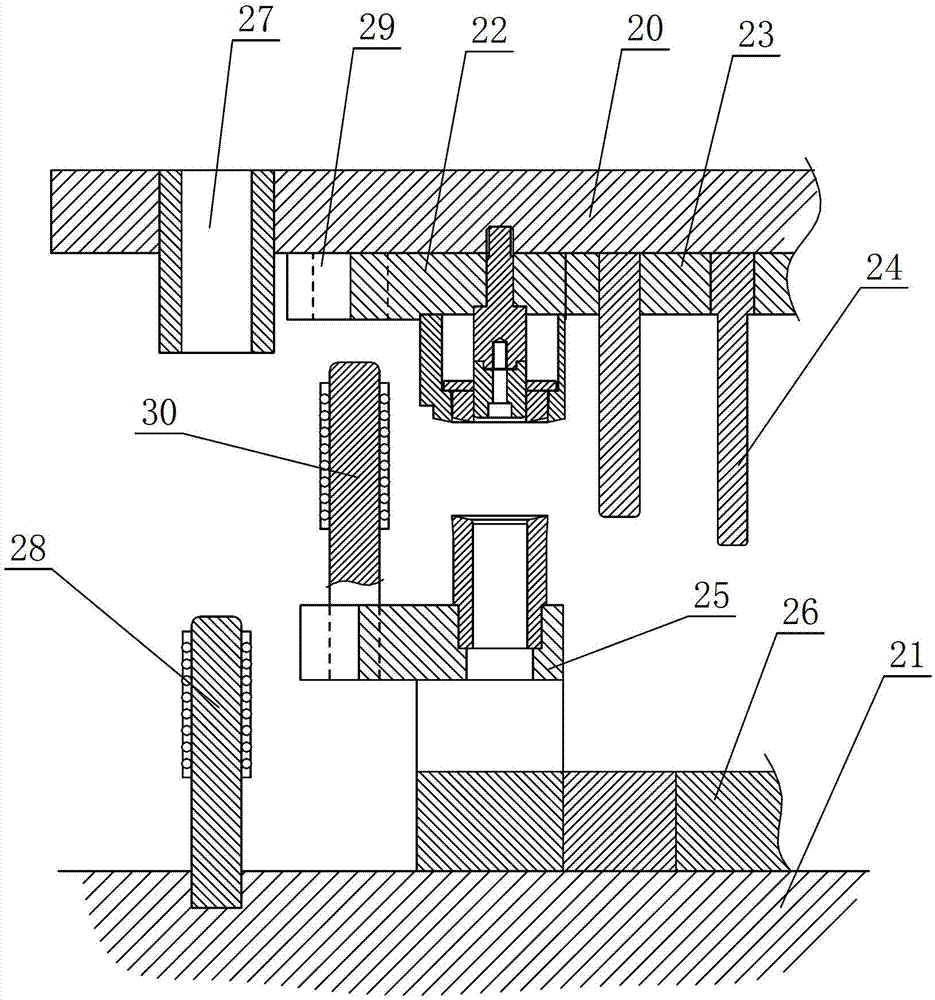
图2是本发明具体实施方式1提供的电池钢壳高精度落料模具结构的结构示意图。Fig. 2 is a schematic structural view of the high-precision blanking die structure for a battery steel case provided in Embodiment 1 of the present invention.
具体实施方式 Detailed ways
下面结合附图并通过具体实施方式来进一步说明本发明的技术方案。The technical solutions of the present invention will be further described below in conjunction with the accompanying drawings and through specific implementation methods.
请参阅图2所示,图2是本发明具体实施方式1提供的电池钢壳高精度落料模具结构的结构示意图。Please refer to FIG. 2 . FIG. 2 is a schematic structural diagram of a high-precision blanking die structure for a battery steel case provided in Embodiment 1 of the present invention.
本实施例中,一种电池钢壳高精度落料模具结构其包括上模架板20和对应设置于上模架板20下方的冲床工作台板21,所述上模架板20的下方安装有落料上模板22和拉伸上模固定板23,所述落料上模板22上安装落料上模,所述拉伸上模固定板23上依次设置有多个平行间隔布置的拉伸冲头24,所述冲床工作台板21上对应落料上模板22、拉伸冲头24设置有落料下模板25和拉伸凹模26,所述落料下模板25上安装落料下模,所述上模架板20与冲床工作台板21之间安装由模架导套27和模架导柱28组成的导向机构,所述落料上模板22上安装落料模导套29,配合落料模导套29于落料下模板25上安装落料模导柱30,所述落料模导柱30、落料模导套29与模架导柱28、模架导套27之间呈纵横两个方向排列。In this embodiment, a high-precision blanking mold structure for battery steel shells includes an upper
上述电池钢壳高精度落料模具结构不仅提高了上下模的配合精度,避免了模具崩刃现象,延长了模具寿命;而且在拆装模具时,只要安装就位就行,不必多次调校上下模位置,简化了安装手续,缩短了维修时间,提高了生产效率。The high-precision blanking mold structure for the battery steel case not only improves the matching accuracy of the upper and lower molds, avoids the phenomenon of mold chipping, and prolongs the life of the mold; moreover, when disassembling the mold, it only needs to be installed in place, and there is no need to adjust the upper and lower molds multiple times. The mold position simplifies the installation procedure, shortens the maintenance time and improves the production efficiency.
以上实施例只是阐述了本发明的基本原理和特性,本发明不受上述事例限制,在不脱离本发明精神和范围的前提下,本发明还有各种变化和改变,这些变化和改变都落入要求保护的本发明范围内。本发明要求保护范围由所附的权利要求书及其等效物界定。The above embodiments have only set forth the basic principles and characteristics of the present invention, the present invention is not limited by the above-mentioned examples, and on the premise of not departing from the spirit and scope of the present invention, the present invention also has various changes and changes, and these changes and changes all fall within the scope of the claimed invention. The protection scope of the present invention is defined by the appended claims and their equivalents.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210533022.5A CN103008480B (en) | 2012-12-11 | 2012-12-11 | A kind of battery steel shell high accuracy blanking die structure |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210533022.5A CN103008480B (en) | 2012-12-11 | 2012-12-11 | A kind of battery steel shell high accuracy blanking die structure |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN103008480A true CN103008480A (en) | 2013-04-03 |
| CN103008480B CN103008480B (en) | 2015-12-02 |
Family
ID=47957895
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201210533022.5A Active CN103008480B (en) | 2012-12-11 | 2012-12-11 | A kind of battery steel shell high accuracy blanking die structure |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN103008480B (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110405055A (en) * | 2019-06-18 | 2019-11-05 | 李可 | Cylindrical battery steel shell automatic stamping production line |
| CN113600685A (en) * | 2021-07-14 | 2021-11-05 | 宁波光华电池有限公司 | Steel shell cup punching compound die |
| CN116786674A (en) * | 2023-08-25 | 2023-09-22 | 常州松田伺服冲床有限公司 | Full-automatic battery box stretching punch press and battery box stretching method |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH10286638A (en) * | 1997-04-14 | 1998-10-27 | Nisshinbo Ind Inc | Press die |
| US20040206150A1 (en) * | 2003-04-15 | 2004-10-21 | Rubalcava Manuel P. | Method and apparatus for forming container bodies |
| CN101708613A (en) * | 2009-12-11 | 2010-05-19 | 广州丰江微电子有限公司 | IC punching die |
| CN201693083U (en) * | 2010-07-09 | 2011-01-05 | 浙江申林汽车部件有限公司 | Punching pressure gear die |
| CN201783574U (en) * | 2010-06-17 | 2011-04-06 | 无锡曙光模具有限公司 | Special die for processing limit plates of refrigerator temperature controllers |
| CN202479347U (en) * | 2011-12-23 | 2012-10-10 | 宝钢发展有限公司劳防用品厂 | Simple stamping die with adjustable template |
| CN202984474U (en) * | 2012-12-11 | 2013-06-12 | 无锡市金杨新型电源有限公司 | High-precision blanking die structure of steel battery shell |
-
2012
- 2012-12-11 CN CN201210533022.5A patent/CN103008480B/en active Active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH10286638A (en) * | 1997-04-14 | 1998-10-27 | Nisshinbo Ind Inc | Press die |
| US20040206150A1 (en) * | 2003-04-15 | 2004-10-21 | Rubalcava Manuel P. | Method and apparatus for forming container bodies |
| CN101708613A (en) * | 2009-12-11 | 2010-05-19 | 广州丰江微电子有限公司 | IC punching die |
| CN201783574U (en) * | 2010-06-17 | 2011-04-06 | 无锡曙光模具有限公司 | Special die for processing limit plates of refrigerator temperature controllers |
| CN201693083U (en) * | 2010-07-09 | 2011-01-05 | 浙江申林汽车部件有限公司 | Punching pressure gear die |
| CN202479347U (en) * | 2011-12-23 | 2012-10-10 | 宝钢发展有限公司劳防用品厂 | Simple stamping die with adjustable template |
| CN202984474U (en) * | 2012-12-11 | 2013-06-12 | 无锡市金杨新型电源有限公司 | High-precision blanking die structure of steel battery shell |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110405055A (en) * | 2019-06-18 | 2019-11-05 | 李可 | Cylindrical battery steel shell automatic stamping production line |
| CN113600685A (en) * | 2021-07-14 | 2021-11-05 | 宁波光华电池有限公司 | Steel shell cup punching compound die |
| CN116786674A (en) * | 2023-08-25 | 2023-09-22 | 常州松田伺服冲床有限公司 | Full-automatic battery box stretching punch press and battery box stretching method |
Also Published As
| Publication number | Publication date |
|---|---|
| CN103008480B (en) | 2015-12-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105251862A (en) | Multi-station aluminum alloy frame stamping die | |
| CN104368697A (en) | Reinforcing plate punching die | |
| CN205439068U (en) | A kind of plastic frame plastic fixture | |
| CN103008480B (en) | A kind of battery steel shell high accuracy blanking die structure | |
| CN202667407U (en) | Protruding pole die replaced and installed quickly | |
| CN102764813A (en) | Punching and blanking compound die for partition plate | |
| CN204353346U (en) | A kind of automobile component incised notch mouth assembling die | |
| CN203778599U (en) | Installation corner brace processing equipment | |
| CN103639266A (en) | Magnetic-conducting piece blanking die | |
| CN206122476U (en) | Novel multifunctional mould for piercing press | |
| CN106694691A (en) | Combined punching die | |
| CN207857660U (en) | A New Type of Continuous Stamping Die for Shrapnel Terminals | |
| WO2018028024A1 (en) | Multi-station progressive die for cover plate | |
| CN205341632U (en) | Punch a hole, typing all -in -one | |
| CN202984474U (en) | High-precision blanking die structure of steel battery shell | |
| CN104511528A (en) | Automatic stamping die | |
| CN204564926U (en) | A kind of processing mold of spacing inserted sheet of controller | |
| CN204584050U (en) | The right installation bracket board forming die of a kind of automobile front axle | |
| CN201960031U (en) | Perforated-plate punching device | |
| CN207698198U (en) | A kind of blanking die mechanism of the flat bubble-cap machine of high speed | |
| CN203197100U (en) | Novel forming die | |
| CN205763262U (en) | Bending mold for back panel | |
| CN203875965U (en) | Paper punching die with alternating copper stators | |
| CN211968547U (en) | Mould embryo subassembly of quick installation | |
| CN204974934U (en) | Punching machine tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CP01 | Change in the name or title of a patent holder | ||
| CP01 | Change in the name or title of a patent holder |
Address after: 214117 No. 6, Gan Lu Gannan Road, Xishan, Wuxi, Jiangsu Patentee after: WUXI JINYANG NEW MATERIAL Co.,Ltd. Address before: 214117 No. 6, Gan Lu Gannan Road, Xishan, Wuxi, Jiangsu Patentee before: WUXI CITY JINYANG NEW TYPE POWER SUPPLY Co.,Ltd. |
|
| CP03 | Change of name, title or address | ||
| CP03 | Change of name, title or address |
Address after: 214000 Jiangsu Province, Xishan District, Ehu Town, Ganlu, Xi Gan Road No. 1 Patentee after: WUXI JINYANG NEW MATERIAL Co.,Ltd. Country or region after: China Address before: 214117 No. 6, Gan Lu Gannan Road, Xishan, Wuxi, Jiangsu Patentee before: WUXI JINYANG NEW MATERIAL Co.,Ltd. Country or region before: China |