WO2024248153A1 - 巻鉄心およびその製造方法 - Google Patents
巻鉄心およびその製造方法 Download PDFInfo
- Publication number
- WO2024248153A1 WO2024248153A1 PCT/JP2024/020114 JP2024020114W WO2024248153A1 WO 2024248153 A1 WO2024248153 A1 WO 2024248153A1 JP 2024020114 W JP2024020114 W JP 2024020114W WO 2024248153 A1 WO2024248153 A1 WO 2024248153A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- steel plate
- wound core
- region
- tensile stress
- stress
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/24—Magnetic cores
- H01F27/245—Magnetic cores made from sheets, e.g. grain-oriented
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/24—Magnetic cores
- H01F27/245—Magnetic cores made from sheets, e.g. grain-oriented
- H01F27/2455—Magnetic cores made from sheets, e.g. grain-oriented using deformed sheets, e.g. bent laminations
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/24—Magnetic cores
- H01F27/25—Magnetic cores made from strips or ribbons
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F3/00—Cores, Yokes, or armatures
- H01F3/02—Cores, Yokes, or armatures made from sheets
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F3/00—Cores, Yokes, or armatures
- H01F3/04—Cores, Yokes, or armatures made from strips or ribbons
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F41/00—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties
- H01F41/02—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties for manufacturing cores, coils, or magnets
- H01F41/0206—Manufacturing of magnetic cores by mechanical means
- H01F41/0233—Manufacturing of magnetic circuits made from sheets
- H01F41/024—Manufacturing of magnetic circuits made from deformed sheets
Definitions
- the present invention relates to a wound core and a method for manufacturing the same.
- Patent Document 2 a low-iron-loss grain-oriented electrical steel sheet is known in which the local stress state inside the steel sheet is controlled to an appropriate condition.
- Patent Document 1 it is difficult to control the size of the extremely fine closure domains, and there is variation in the size of the closure domains, so the effect is not complete. Furthermore, the technology described in Patent Document 2 also does not take into account the influence of the joints between the steel sheets in the wound core, leaving room for improvement.
- the objective of this disclosure is to provide a wound core and a manufacturing method thereof that can appropriately control the local stress state inside the steel plate formed near the joint and reduce iron loss.
- the gist of this disclosure is as follows:
- a wound core having a wound shape formed by laminating folded steel plates The wound core has four flat portions and four corner portions adjacent to the flat portions in a side view of the wound shape seen from a direction along the surface of the steel plate, It is formed in a rectangular shape with a hollow part in the center, Each layer of the steel plate has at least one joint where ends in the winding direction are butted together, A gap exists between the opposing ends of the steel plates at the joint of each steel plate, A wound core, in which a tensile stress of 10 MPa or more is introduced in the thickness direction of the steel plate at one or more locations in a predetermined region defined according to the positional relationship between the gap of a steel plate and the gap of a steel plate stacked adjacent to the arbitrary steel plate in a cross section perpendicular to the surface of the steel plate and along the winding direction.
- This disclosure provides a wound core and a manufacturing method thereof that can appropriately control the local stress state inside the steel plate formed near the joint and reduce iron loss.
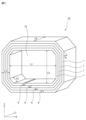
- FIG. 2 is a perspective view showing a schematic diagram of one embodiment of a wound core.
- FIG. 2 is a side view of the wound core shown in the embodiment of FIG. 1;
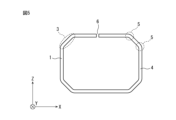
- FIG. 4 is a side view showing a schematic diagram of another embodiment of a wound core.
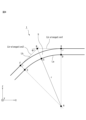
- FIG. 2 is a diagram showing a schematic diagram of an example of a bent portion (curved portion) of a grain-oriented electrical steel sheet.
- FIG. 2 is a diagram showing a schematic diagram of an example of one layer of grain-oriented electromagnetic steel sheet in a wound core body.
- FIG. 2 is a diagram showing a schematic diagram of an example of one layer of grain-oriented electromagnetic steel sheet in a wound core body.
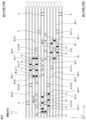
- FIG. 4 is a schematic diagram showing the detailed shape and arrangement of the joints in region A1 or region A2 of FIG.
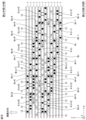
- FIG. 7B is a schematic diagram for explaining a region M in which a region in which tensile stress is introduced in the plate thickness direction is provided for all the joints in FIG. 7A .
- FIG. 2 is a schematic diagram showing a cross section of a steel sheet, and is a diagram showing a state in which regions in which tensile stress is introduced in the sheet thickness direction are provided periodically in the X-axis direction (winding direction).
- FIG. 2 is a perspective view of a steel plate, and is a diagram showing a schematic state in which a region in which tensile stress is introduced in the plate thickness direction is provided in a direction intersecting the winding direction (Y-axis direction perpendicular to the winding direction).
- FIG. 13 is a diagram for explaining the effect of providing a region in which tensile stress is introduced in the plate thickness direction.
- FIG. 13 is a diagram for explaining the effect of providing a region in which tensile stress is introduced in the plate thickness direction.
- FIG. 1 is a schematic diagram of an apparatus for manufacturing a wound core in the form of a unicore;
- FIG. 4 is a diagram for explaining detailed dimensions of a wound core.
- grain-oriented electromagnetic steel sheet may be referred to simply as “steel sheet” or “electromagnetic steel sheet”
- wound core may be referred to simply as “wound core body” or “iron core.”
- the wound core according to one embodiment of the present invention is a wound core formed by stacking folded steel sheets, and has a rectangular structure with a hollow section at the center, with four flat sections and four corner sections adjacent to the flat sections, when viewed from the side of the wound shape from the direction along the surface of the steel sheets.
- the flat sections refer to the straight line parts other than the bent sections.
- the inner surface side curvature radius r in the side view of the bent sections is, for example, 1.0 mm or more and 5.0 mm or less.
- the grain-oriented electromagnetic steel sheet has a chemical composition containing, by mass%, 2.0 to 7.0% Si, with the balance being Fe and impurities, and has a texture oriented in the Goss direction.
- a grain-oriented electromagnetic steel strip described in JIS C 2553:2019 can be used as the grain-oriented electromagnetic steel sheet.
- the shapes of the wound core and grain-oriented electromagnetic steel sheet according to one embodiment of the present invention will be specifically described.
- the shapes of the wound core and grain-oriented electromagnetic steel sheet described here are not particularly new, but merely conform to the shapes of known wound cores and grain-oriented electromagnetic steel sheets.
- FIG. 1 is a perspective view showing a schematic representation of one embodiment of a wound core.
- FIG. 2 is a side view of the wound core shown in the embodiment of FIG. 1, showing a side view of the wound core.
- FIG. 3 is a side view showing a schematic representation of another embodiment of the wound core.
- a side view refers to the winding shape of the wound core viewed from a direction along the surface of the steel sheet, and more specifically, refers to the winding core viewed from the axial direction of the windings of the wound core (perpendicular to the plane of the paper in Figure 2).
- a side view refers to a view in the width direction (Y-axis direction in Figure 1) of the long grained electrical steel sheet that constitutes the wound core.
- a side view is a diagram that shows the shape as seen from the side (a diagram in the Y-axis direction in Figure 1).
- the wound core 10 comprises a wound core body that is approximately polygonal in side view.
- the wound core body 10 has a laminated structure in which directional electromagnetic steel sheets 1 are stacked in the sheet thickness direction, and is approximately rectangular in side view.
- the wound core body 10 may be used as a wound core as is, or may be equipped with a known fastener such as a cable tie to secure the stacked directional electromagnetic steel sheets together as needed.
- the core length of the wound core body 10 there is no particular restriction on the core length of the wound core body 10. If the number of bent portions 5 is the same, even if the core length of the wound core 10 changes, the volume of the bent portions 5 is constant, so the iron loss generated at the bent portions 5 is constant. The longer the core length, the smaller the volume ratio of the bent portions 5 to the wound core body 10, and the smaller the impact on iron loss degradation. Therefore, the longer the core length of the wound core body 10, the better.
- the core length of the wound core body 10 is preferably 1.5 m or more, and more preferably 1.7 m or more.
- the core length of the wound core body 10 refers to the circumferential length at the center point of the wound core body 10 in the lamination direction when viewed from the side. Such a wound core can be suitably used for any of the conventionally known applications.
- the iron core according to this embodiment is characterized by its approximately polygonal shape when viewed from the side.
- an iron core with an approximately rectangular (quadrature) shape which is a common shape, will be described; however, iron cores of various shapes can be manufactured by changing the angle and number of bends 5 and the length of the flat surfaces. For example, if the angle of all bends 5 is 45° and the length of the flat surfaces 4 is equal, the side view will be octagonal. On the other hand, if there are six bends 5 with an angle of 60° and the length of the flat surfaces 4 is equal, the side view will be hexagonal.
- the wound core body 10 includes a portion in which directional electromagnetic steel sheets 1, in which flat portions 4, 4a and bent portions 5 are alternately arranged in the longitudinal direction, are stacked in the sheet thickness direction, and has a laminated structure 2 having a generally rectangular shape in side view and a hollow portion 15.
- the corner portion 3 including the bent portions 5 has two or more bent portions 5 having a curved shape in side view, and the sum of the bending angles of the bent portions 5 present in one corner portion 3 is, for example, 90°.
- the corner portion 3 has a flat portion 4a between adjacent bent portions 5, 5 that is shorter than the flat portion 4. Therefore, the corner portion 3 has two or more bent portions 5 and one or more flat portions 4a.
- one bent portion 5 is 45°.
- one bent portion 5 is 30°.
- the wound core of this embodiment can be configured with bent portions having various angles, but from the standpoint of suppressing the occurrence of distortion due to deformation during processing and suppressing iron loss, the bending angle ⁇ ( ⁇ 1, ⁇ 2, ⁇ 3) of the bent portion 5 is preferably 60° or less, and more preferably 45° or less.
- the design can be selected arbitrarily based on the points that are important in core processing.
- FIG. 4 is a diagram showing an example of a bend (curved portion) 5 of a grain-oriented electromagnetic steel sheet 1.
- the bending angle of the bend 5 means the angle difference between the straight portion on the rear side of the bending direction and the straight portion on the front side of the bending direction in the grain-oriented electromagnetic steel sheet, and is expressed as the angle ⁇ , which is the supplementary angle of the angle formed by two imaginary lines Lb-elonation1 and Lb-elonation2 obtained by extending the straight portions that are the surfaces of the flat portions 4, 4a on both sides that sandwich the bend 5 on the outer surface of the grain-oriented electromagnetic steel sheet 1.
- the points where the extended straight lines depart from the steel sheet surface are the boundaries between the flat portions 4 and the bend 5 on the outer surface of the steel sheet, and are points F and G in FIG. 4.
- the bent portion 5 is the portion of the grain-oriented electrical steel sheet 1 that is surrounded by the above-mentioned points D, E, F, and G when viewed from the side of the grain-oriented electrical steel sheet 1.
- the steel sheet surface between points D and E, i.e., the inner surface of the bent portion 5, is shown as La
- the steel sheet surface between points F and G, i.e., the outer surface of the bent portion 5 is shown as Lb.
- This figure also shows the inner radius of curvature r of bend 5 when viewed from the side.
- the radius of curvature r of bend 5 is obtained by approximating La with an arc passing through points E and D. The smaller the radius of curvature r, the sharper the curve of the curved portion of bend 5, and the larger the radius of curvature r, the gentler the curve of the curved portion of bend 5.
- the radius of curvature r at each bend 5 of each grain-oriented electromagnetic steel sheet 1 stacked in the sheet thickness direction may have a certain degree of variation. This variation may be due to forming accuracy, and it is also possible that unintended variation occurs due to handling during stacking. Such unintended errors can be suppressed to about 0.2 mm or less in current normal industrial manufacturing. If such variation is large, a representative value can be obtained by measuring the radius of curvature for a sufficiently large number of steel sheets and averaging them. It is also possible to intentionally change the radius for some reason, but the present invention does not exclude such a form.
- the radius of curvature r of the bend 5 (the inner radius of curvature of the bend 5 in a side view) is preferably 1 mm or more and 5 mm or less. By setting the radius of curvature r to 1 mm or more and 5 mm or less, the building factor (BF) can be further suppressed.
- the method for measuring the radius of curvature r of the bent portion 5 can be measured, for example, by observing at 200x using a commercially available microscope (Nikon ECLIPSE LV150). Specifically, the center of curvature A is found from the observation results. For example, if the intersection point A is defined as the intersection point of line segments EF and DG extended inwardly on the opposite side to point B, then the magnitude of the radius of curvature r corresponds to the length of line segment AC.
- the intersection point on the circular arc DE on the inside of the bent portion of the steel plate is defined as C.
- FIGS. 5 and 6 are schematic diagrams showing an example of one layer of directional electromagnetic steel sheet 1 in the wound core body.
- the directional electromagnetic steel sheet 1 used in the examples of FIG. 5 and FIG. 6 is folded to realize a wound core in a unicore form, and has two or more bent portions 5 and a flat portion 4, and forms a substantially polygonal ring in side view via joints 6 (gaps) that are the longitudinal end faces of one or more directional electromagnetic steel sheets 1.
- the wound core body 10 may have a laminated structure that is generally polygonal in side view as a whole.
- one directional electromagnetic steel sheet may constitute one layer of the wound core body via one joint 6 (one directional electromagnetic steel sheet is connected via one joint 6 for each turn), or as shown in the example of FIG. 6, one directional electromagnetic steel sheet 1 constitutes approximately half the circumference of the wound core, and two directional electromagnetic steel sheets 1 constitute one layer of the wound core body via two joints 6 (two directional electromagnetic steel sheets 1 are connected to each other via two joints 6 for each turn).
- the thickness of the grain-oriented electrical steel sheet 1 used in this embodiment is not particularly limited and may be selected appropriately depending on the application, etc., but is usually in the range of 0.15 mm to 0.35 mm, and preferably in the range of 0.18 mm to 0.27 mm.
- one joint 6 of one grain-oriented electromagnetic steel sheet that constitutes one layer of the wound core body is located in area A1 shown in Figures 2 and 3.
- two joints 6 of two grain-oriented electromagnetic steel sheets that constitute one layer of the wound core body are located in areas A1 and A2 shown in Figures 2 and 3. Note that detailed shapes and arrangements of joints 6 in area A1 or area A2 are omitted from Figures 2 and 3.
- FIG. 7A is a schematic diagram for explaining the detailed shape and arrangement of the joints 6 in region A1 or region A2 in FIG. 2 or FIG. 3, and the region where a region 12 where tensile stress is introduced in the sheet thickness direction is provided for a specific joint.
- FIG. 7A shows a schematic cross section perpendicular to the surface of the steel sheet and along the winding direction. As shown in FIG. 7A, the positions of the respective joints 6 (gaps in the joints 6 are shown as 6(n-1), 6(n) ..., etc. in FIG. 7A) of the grain-oriented electrical steel sheets 1 constituting each layer are shifted in the X-axis direction along which the planar portion 4 extends.
- FIG. 7A particularly shows a state in which the joints 6 are arranged at periodically shifted positions in the X-axis direction.
- the wound core body 10 having the joints 6 is excellent in productivity and ease of shape design.
- the presence of the joints 6 means that the steel plate is cut at the joints 6, which can cause iron loss and noise to increase.
- the inventors have thoroughly studied the effect of the stress state inside the steel plate on the core characteristics, and have found that controlling the tensile stress in the thickness direction of the steel plate is particularly effective in reducing iron loss in a wound core having a joint 6. Based on this knowledge, in this embodiment, the stress state (strain distribution) inside the steel plate is controlled in the vicinity of the joint 6 of the wound core. Although the mechanism itself is not completely clear at this point, the inventors' thorough study has led to the deduction that the tensile stress in the thickness direction makes it easier for the magnetic flux passing through the steel plate to bend in the thickness direction. Since the steel plate is interrupted at the joint 6 of the wound core 10, the magnetic flux needs to pass through the gap at the joint 6.
- the magnetic flux which is prevented from progressing in the in-plane direction by the gaps in the joints 6 in the in-plane direction, can be transferred smoothly to the adjacent steel plates that are stacked and in contact with each other. In other words, it is believed that the transfer of magnetic flux to the adjacent steel plates occurs smoothly.
- the grain-oriented electrical steel sheet 1 is provided with a continuous region 12 (hereinafter also referred to as stress region 12) in which a tensile stress of 10 MPa or more is introduced in the sheet thickness direction.
- the stress value inside the sheet thickness was measured by X-ray diffraction to measure the distortion of the crystal lattice in three directions, and the stress values in the rolling direction, sheet thickness direction, and sheet width direction were obtained using material properties such as elastic modulus.
- the crystal distortion in these three directions can be obtained by irradiating the steel sheet with X-rays and detecting and evaluating the reflected X-rays and the transmitted X-rays.
- the steel sheet (test piece) is scanned while moving, and the distortion in the sheet thickness direction is obtained by evaluating the shift amount of the diffraction angle (2 ⁇ ) of the reflected X-ray diffraction peak by the reflection method.
- the distortion in the rolling direction and sheet width direction is obtained by evaluating the shift amount of the diffraction angle of the transmitted X-ray diffraction peak by the transmission method.
- the conversion from strain to stress value can be done by the relational equation between stress and strain in three directions according to the material properties (Young's modulus, Poisson's ratio).
- the stress regions 12 are basically provided near the joints 6 of each steel plate, and when focusing on any one void 6, it is preferable to determine the region in which the stress region 12 should be located, including multiple steel plates adjacent in the stacking direction.
- the region in which the stress region 12 should be located (hereinafter also referred to as the stress placement region) is described in detail below.
- the stress distribution area is set to a region at least twice the thickness of the steel plate from the end of the steel plate member constituting the wound core in the in-plane direction.
- the end of the steel plate member in the in-plane direction is generally formed by shear processing, and is therefore significantly plastically deformed, and there is a high possibility that it will become an unfavorable stress state for the stress area 12 intended by the present application.
- the stress distribution area excludes such end areas.
- One of the end areas is the surface in the Y-axis direction in the wound core of FIG. 1, that is, the area from the surface when the wound core is viewed from the side to the inside of the steel plate (Y-axis direction) up to twice the thickness of the plate.
- the other is the area from the end of the steel plate that faces the joint 6 of the wound member, forming a gap, to the inside of the steel material (X-axis direction in FIG. 6) up to twice the thickness of the plate.
- one method for this is to remove the end area by a method that is less likely to cause distortion, such as electric discharge processing or edge pickling.
- Figure 7A is a schematic diagram of a cross section of the joint 6 of the wound core 10 along the XZ plane at a distance of more than twice the plate thickness from the Y-axis direction end of the wound core 10 toward the inside of the steel material.
- the "cross section at a distance of more than twice the plate thickness toward the inside of the steel material” is intended to avoid the end region mentioned above.
- the gap between the opposing ends of the steel plates at the joint 6 formed by cutting the steel plates is 6(n).
- position An the position that is twice the plate thickness in the positive direction of the X axis from the end of the gap 6(n) on the positive side of the X axis is defined as position An
- position Bn the position that is twice the plate thickness in the negative direction of the X axis from the end of the gap 6(n) on the negative side of the X axis.
- stress distribution areas M(n) are defined on both sides of the X-axis and Z-axis.
- the range in the Z-axis direction of the stress distribution area M(n) based on the gap 6(n) is a range of three steel plates, including the (n-1)th steel plate, the nth steel plate, and the (n+1)th steel plate from the inside.
- the stress distribution area M(n) is meaningless in areas where no steel plates exist
- the range of the stress placement area on the positive side of the X-axis based on the void 6(n) is the range from position An to either position B(n-1) or position B(n+1) which is located on the positive side of the X-axis from position An and which is closer to position An.
- the range of the stress placement area on the negative side of the X-axis based on the void 6(n) is the range from position Bn to either position A(n-1) or position A(n+1) which is located on the negative side of the X-axis from position Bn and which is closer to position Bn.
- the range of the stress placement area on the positive side of the X-axis is the same distance from position An as the range of the stress placement area on the negative side of the X-axis.
- the range of the stress distribution area on the negative side of the X-axis is set to the same distance from position Bn as the range of the stress distribution area on the positive side of the X-axis.
- FIG. 7A the stress distribution regions M(n), M(n+3), and M(n+7) based on voids 6(n), 6(n+3), and 6(n+7) determined according to the above definition are shown with hatching.
- the area from the opposing steel plate ends that form a gap at joint 6 to twice the plate thickness in the X-axis direction is the end area described above, and is excluded from the stress distribution area, so it is not hatched.
- FIG. 7B is a schematic diagram for explaining the area M where the area where tensile stress is introduced in the plate thickness direction is provided for all joints 6 in FIG. 7A.
- the stress distribution area M(n) based on a specific void 6 e.g., void 6(n)
- the stress distribution area M(n+1) will have a portion with the same range in the X-axis direction as the stress distribution area M(n+1) based on the void 6 of the steel plate adjacent in the Z-axis direction (void 6(n+1) in FIG. 7B).
- FIG. 7B the area where the stress distribution areas M overlap partially is shown with cross-hatching.
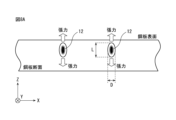
- FIG. 8A is a schematic diagram showing a cross section of a steel plate, and shows a state in which multiple stress regions 12 are provided in the X-axis direction (winding direction).
- the stress regions 12 may be provided at a predetermined interval in the X-axis direction in the cross section of the steel plate, in other words, the stress regions 12 may be provided periodically. Therefore, the stress regions 12 are provided in the stress distribution region M, but may also be provided over the entire area of the steel plate other than the stress distribution region M.
- the width D in the X-axis direction (width in the winding direction) of the stress region 12 is preferably 1.4 mm or less.
- the width D is preferably 0.3 to 1.1 mm, and more preferably 0.7 to 1.1 mm.
- the length L in the Z-axis direction is preferably 0.2*t ⁇ L ⁇ t, where t is the thickness of the steel plate.
- the length L is more preferably 0.4*t ⁇ L ⁇ 0.8*t. If the width D is 1.4 mm or more, the position of the magnetic flux transfer will vary widely in the X-axis direction, increasing iron loss. Furthermore, if the length L in the Z-axis direction is too short, the effect of the magnetic flux transfer will not be achieved. Therefore, it is preferable that the width D and length L are in the above range.
- the maximum stress in the stress region 12 is preferably present at a depth of more than 10 ⁇ m from the surface of the steel sheet. If it is present in an area shallower than 10 ⁇ m, the bending of the magnetic flux when it is transferred becomes steeper, resulting in increased thin current loss and reduced iron loss reduction effect. Therefore, the maximum stress in the stress region 12 is present at a depth of more than 10 ⁇ m from the surface of the steel sheet, preferably 30 to 80 ⁇ m, and more preferably 40 to 70 ⁇ m.
- the interval between the stress regions 12 in the X-axis direction affects the magnetic domain subdivision due to the interaction between adjacent stress regions 12, so if the interval is too large, the effect of reducing iron loss is reduced.
- the interval between the stress regions 12 is preferably 10.0 mm or less, and more preferably 7.0 mm or less.
- the interval between the stress regions 12 is about 5 mm, but on the other hand, the stress regions 12 also become an obstacle to the magnetic flux in the in-plane direction of the steel plate (magnetization direction), and if the interval is too narrow, it can also cause an increase in iron loss, so the interval between the stress regions 12 in the X-axis direction is preferably 2 mm or more.
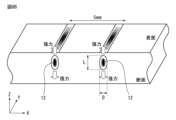
- FIG. 8B is a perspective view of a steel plate, and is a diagram showing a schematic state in which the stress region 12 is provided in a direction intersecting the winding direction (Y-axis direction perpendicular to the winding direction in FIG. 8B).
- the stress region 12 may extend in a direction intersecting the winding direction and be provided so as to cross the winding direction.
- the stress region 12 may be provided continuously in the direction intersecting the winding direction, or may be provided periodically at a predetermined interval.
- the stress region 12 preferably extends in a direction that forms an angle of 60 to 120° with respect to the X-axis direction in a field of view along the Z-axis. More preferably, it extends in a direction that forms an angle of 80 to 110°.
- the stress region 12 is defined as a continuous region in which the tensile stress in the plate thickness direction is 10 MPa or more. If the tensile stress in the plate thickness direction is less than 10 MPa, the effect of the magnetic permeability is small compared to the gap in the joint 6, and therefore the effect of providing the region 12 in which the tensile stress is introduced cannot be fully obtained.
- the maximum value of the tensile stress in the plate thickness direction is equal to or less than the yield stress of the steel plate, which is the material. If the maximum value of the tensile stress becomes large, the plastic region increases, and the decrease in magnetic permeability due to plastic strain becomes significant, resulting in worsening of iron loss. In general, the point at which the stress state changes significantly from the elastic region to the plastic region can be determined by the yield stress of the material.
- the maximum value of the tensile stress in the plate thickness direction in the stress region 12 is equal to or less than the yield stress value of the material.
- the maximum value of the tensile stress is more preferably 80 to 200 MPa.
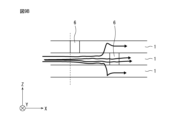
- FIGS. 9A and 9B are diagrams for explaining the effect of providing a stress region 12. As mentioned above, it should be noted that the explanation of FIG. 9A and FIG. 9B is one possibility regarding the mechanism of action of the present invention. In FIG. 9A, the arrows indicate the flow of magnetic flux when a stress region 12 is provided.
- the stress region 12 and the stress distribution region M are defined as described above.
- the effect of the invention is achieved by the presence of the stress region 12 within the stress distribution region M.
- the effect of the invention is achieved even if only a part of the steel plates among the laminated steel plates overlaps with the stress distribution region M.
- the degree of overlap of the above regions is preferably 0.1% or more, where Ptot is the total area of the stress distribution region M within the observation region and PM is the total area of the stress region 12 within the stress distribution region M when observing a region that is 1/2 the laminate thickness in the Z-axis direction and 1/2 the laminate thickness in the X-axis direction. If PM/Ptot is less than 0.1%, the effect of the invention is not sufficient. It is preferably 2% or more, and more preferably 5% or more.
- the stress region 12 is an obstacle to the magnetic flux in the in-plane direction (magnetization direction) of the steel sheet, so if there is an excessive amount of stress region 12 in the stress distribution region M, it can cause iron loss deterioration. For this reason, it is preferable that PM/Ptot is 40% or less, and more preferably 30% or less.
- the degree of this overlap is defined as the ratio of the number of steel plates SM in which a stress region 12 exists within the stress distribution region M to the total number of stacked steel plates Stot for the stacked steel plates.
- a steel plate in which a stress region 12 exists within the stress distribution region M is a steel plate in which at least one stress region 12 exists within at least one stress distribution region M.
- SM/Stot is preferably 1% or more, and more preferably 2% or more. It is preferably 5% or more, and even more preferably 10% or more. Of course, it is preferable that 100% of the stress regions 12 exist within the stress distribution region M in all steel plates.
- the stress region 12 can be an obstacle to the magnetic flux in the in-plane direction of the steel plate and can cause iron loss deterioration, the stress region 12 is provided only within the stress distribution region M, and it is not necessary that the stress region 12 is provided outside the stress distribution region M. In other words, tensile stress may be introduced only in the stress distribution region M.
- the winding direction of the wound core may be the rolling direction of the steel plate.
- the winding direction of the wound core may be the ⁇ 110 ⁇ 001> direction of the steel plate.
- the X-axis direction may be the rolling direction of the steel plate or the ⁇ 110 ⁇ 001> direction of the steel plate.
- the method for manufacturing the grain-oriented electrical steel sheet is not particularly limited, and a conventional method for manufacturing grain-oriented electrical steel sheet may be appropriately selected.
- a preferred example of the manufacturing method is to heat a slab having 0.04 to 0.1 mass% C and the other chemical composition of the grain-oriented electrical steel sheet to 1000°C or higher and perform hot rolling, followed by hot-rolled sheet annealing as necessary, and then cold rolling once or two or more times with intermediate annealing to form a cold-rolled steel sheet, and then heating the cold-rolled steel sheet to 700 to 900°C in a wet hydrogen-inert gas atmosphere to perform decarburization annealing, and further nitriding annealing as necessary, applying an annealing separator, performing finish annealing at about 1000°C, and forming an insulating coating at about 900°C.
- the wound core composed of the grain-oriented electromagnetic steel sheet 1 having the above-mentioned configuration is formed by stacking the grain-oriented electromagnetic steel sheets 1 that have been individually bent and processed in layers and assembling them into a wound shape, and multiple grain-oriented electromagnetic steel sheets 1 are connected to each other via at least one joint 6 for each turn.
- the method of introducing tensile stress in the thickness direction inside the grain-oriented electrical steel sheet is, for example, a method of irradiating with a laser or electron beam, and by irradiating in a medium in which the viscosity (mPa ⁇ s) of the aqueous solution is 2 to 8, vibration of the steel sheet caused by irradiation with the laser or electron beam is reduced, making it easier to obtain the desired stress distribution. If the viscosity exceeds 8, it becomes difficult to introduce stress.
- a method in which the viscosity is controlled by the concentration and temperature of the aqueous solution is preferable because the conditions can be adjusted appropriately. For example, a method using an aqueous ethanol solution with a concentration of 40 to 60% at a temperature of -10°C to 20°C is one preferred example.
- tensile stress may be introduced at the coil stage before the steel sheet is cut in the rolling direction, or at the time of bending.
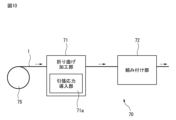
- FIG. 10 shows a schematic diagram of a manufacturing device 70 for wound cores in the form of a unicore.
- This manufacturing device 70 includes a folding section 71 that individually folds grain-oriented electromagnetic steel sheets 1, and may also include an assembly section 72 that stacks the folded grain-oriented electromagnetic steel sheets 1 in layers and assembles them into a wound shape to form a wound core that includes a portion where grain-oriented electromagnetic steel sheets 1, in which flat sections 4 and bent sections 5 are alternately continuous in the longitudinal direction, are stacked in the sheet thickness direction.
- the directional electromagnetic steel sheet 1 is fed to the bending section 71 by being unwound at a predetermined conveying speed from a steel sheet supply section 75, which holds a hoop material formed by winding the directional electromagnetic steel sheet 1 into a roll.
- the directional electromagnetic steel sheet 1 fed in this manner is cut to an appropriate size in the bending section 71 and is then subjected to a bending process in which the sheet is individually folded in small batches, such as one by one.
- the bending processing portion 71 includes a tensile stress introduction portion 71a.
- the tensile stress introduction portion 71a introduces tensile stress into the directional electromagnetic steel sheet 1 before cutting the directional electromagnetic steel sheet 1 or during bending processing after cutting the directional electromagnetic steel sheet 1 by the method described above.
- the stress distribution region M in each grain-oriented electromagnetic steel sheet 1 is determined in the design based on the planned position of each grain-oriented electromagnetic steel sheet 1 when the grain-oriented electromagnetic steel sheets 1, in which the flat portions 4 and the curved portions 5 are alternately continuous, are stacked in the sheet thickness direction. For this reason, it is possible to introduce tensile stress only to the stress distribution region M by irradiating a laser, electron beam, etc., to the planned position that will become the stress distribution region M in the design in each grain-oriented electromagnetic steel sheet 1.
- the radius of curvature of the bent portion 5 caused by the bending process is extremely small, and therefore the processing strain imparted to the grain-oriented electrical steel sheet 1 by the bending process is extremely small. In this way, while it is expected that the density of the processing strain will be large, if the volume affected by the processing strain can be reduced, the annealing process can be omitted.
- a laser irradiation method is used to introduce tensile stress into the steel plate.
- the steel plate is irradiated with a laser in ethanol at a temperature of about 3°C to 15°C to introduce tensile stress into the steel plate.
- the steel plate is also irradiated with a laser in air, in water at 24°C, and in ethanol at 24°C to introduce tensile stress into the steel plate.
- the beam diameter was set to 150 ⁇ m under all conditions, the output was appropriately adjusted, and the laser was irradiated in advance onto the steel plate area corresponding to the joint 6.
- the steel plates thus obtained are A, B, C, D, D-2, E, F, G, H, I, J, K, L, M, M-2, M-3, M-4, N, O, P, Q, R, S, T, U, V, W, Z, AA, BB, CC, CC-2, CC-3, CC-4, CC-5, CC-6, DD, EE, FF, and GG, as shown in Table 1 below.
- a wound core was then created from the steel plates shown in Table 1. Detailed dimensions of the wound core are shown in Figure 11 and Table 2.
- the lap length in Table 2 indicates the distance between two adjacent joints 6 in the X-axis direction (for example, the length from the end of gap 6(n) on the positive side of the X-axis to the end of gap 6(n-1) on the negative side of the X-axis shown in Figure 7A).
- the number of steps is the number of steel plates by which the joints 6 are periodically shifted in the X-axis direction ("6" in Figure 7A).
- the iron loss at 50 Hz and magnetic flux density of 1.7 T was measured by the excitation current method.
- the iron loss ratio was low for test Nos. 8 to 55, in which a tensile stress of 10 MPa or more was introduced, while the iron loss ratio was high for test Nos. 1 to 7, in which a tensile stress of less than 10 MPa was introduced.
- the iron loss ratio was 1.14 or less for steel sheets B, C, D, D-2, E, F, G, H, I, J, K, L, M, M-2, M-3, M-4, N, O, P, Q, R, S, T, U, V, W, Z, AA, BB, CC, CC-2, CC-3, CC-4, CC-5, CC-6, DD, EE, FF, and GG, in which a tensile stress of 10 MPa or more was introduced in the thickness direction.
- steel plate A where a tensile stress of 10 MPa or more was not introduced in the plate thickness direction, the iron loss ratio exceeded 1.14.
- the iron loss ratio of the invention examples in which SM/Stot was 2% or more was lower than that of the invention examples in which SM/Stot was less than 2%, and the iron loss ratio decreased significantly as SM/Stot increased.
Landscapes
- Engineering & Computer Science (AREA)
- Power Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Soft Magnetic Materials (AREA)
- Manufacturing Cores, Coils, And Magnets (AREA)
Abstract
Description
前記巻鉄心は、前記鋼板の面に沿った方向から前記巻回形状を見た側面視において、平面部と、前記平面部に隣接するコーナー部とをそれぞれ四つ有することにより、
中心に中空部を有する矩形形状に形成され、
前記鋼板は一層毎に巻回方向の端部同士が突合せられた接合部を少なくとも1つ有し、
一層毎の前記鋼板の前記接合部において鋼板の相対する端部の間に空隙が存在し、
前記鋼板の面と直交し且つ前記巻回方向に沿った断面において、任意の鋼板の前記空隙と前記任意の鋼板に隣接して積層された鋼板の前記空隙との位置関係に応じて規定される所定領域において、1箇所または複数箇所に鋼板の板厚方向に10MPa以上の引張応力が導入された、巻鉄心。
鋼板を折り曲げ加工する工程と、
鋼板を切断する工程と、
折り曲げられ、且つ切断された前記鋼板を層状に積み重ね、巻回方向の端部同士を突き合わせて巻回形状に組み付ける工程と、
前記端部の近傍において、又は切断前の前記端部となる位置の近傍において、板厚方向に引張応力を導入する工程と、
を備える、巻鉄心の製造方法。
このような巻鉄心は、従来公知のいずれの用途にも好適に用いることができる。
2 積層構造
3 コーナー部
4,4a 平面部
5 屈曲部
6 接合部
10 巻鉄心
12 領域
15 中空部
70 製造装置
71 加工部
71a 引張応力導入部
72 組み付け部
75 鋼板供給部
Claims (14)
- 折り曲げられた鋼板を積層してなる巻回形状の巻鉄心であって、
前記巻鉄心は、前記鋼板の面に沿った方向から前記巻回形状を見た側面視において、平面部と、前記平面部に隣接するコーナー部とをそれぞれ四つ有することにより、
中心に中空部を有する矩形形状に形成され、
前記鋼板は一層毎に巻回方向の端部同士が突合せられた接合部を少なくとも1つ有し、
一層毎の前記鋼板の前記接合部において鋼板の相対する端部の間に空隙が存在し、
前記鋼板の面と直交し且つ前記巻回方向に沿った断面において、任意の鋼板の前記空隙と前記任意の鋼板に隣接して積層された鋼板の前記空隙との位置関係に応じて規定される所定領域において、1箇所または複数箇所に鋼板の板厚方向に10MPa以上の引張応力が導入された、巻鉄心。 - 一層毎の前記鋼板の前記接合部は前記平面部に配置され、各層の前記鋼板の前記接合部は前記平面部の延在する方向において周期的にずれて配置された、請求項1に記載の巻鉄心。
- 鋼板が積層された巻鉄心において、前記所定領域内に前記板厚方向の引張応力が導入されている鋼板の枚数をSM、全積層枚数をStotとしたとき、SM/Stotが1%以上である、請求項1又は2に記載の巻鉄心。
- 鋼板が積層された巻鉄心において、前記所定領域内に前記板厚方向の引張応力が導入されている領域の面積をPM、前記所定領域の総面積をPtotとしたとき、PM/Ptotが0.1%以上である、請求項1又は2に記載の巻鉄心。
- 前記引張応力は、その最大値が前記鋼板の降伏応力以下である、請求項1又は2に記載の巻鉄心。
- 前記鋼板の面と直交し且つ前記巻回方向に沿った前記断面において、前記引張応力が導入された領域は、一つの該領域の前記巻回方向の幅が1.4mm以下であることを特徴とする、請求項1又は2に記載の巻鉄心。
- 前記鋼板の面と直交し且つ前記巻回方向に沿った前記断面において、前記引張応力が導入された領域は、一つの該領域の板厚方向長さが板厚の0.2倍以上1倍以下であることを特徴とする、請求項1又は2に記載の巻鉄心。
- 前記鋼板の面と直交し且つ前記巻回方向に沿った前記断面において、前記引張応力が導入された領域について、前記巻回方向に隣接する該領域同士の間隔が2mm以上10mm以下である、請求項1又は2に記載の巻鉄心。
- 前記引張応力が導入された領域について、前記引張応力が最大となる点が素材の鋼板表面から10μmより深くに存在することを特徴とする請求項1又は2に記載の巻鉄心。
- 前記引張応力が導入された領域は、前記鋼板の前記巻回方向と交差する方向に連続的または所定間隔で延在し、前記巻回方向を横断するように設けられる、請求項1又は2に記載の巻鉄心。
- 前記巻回方向は前記鋼板の{110}<001>方向と一致する、請求項1又は2に記載の巻鉄心。
- 前記巻回方向は前記鋼板の圧延方向と一致する、請求項1又は2に記載の巻鉄心。
- 前記鋼板の面と直交し且つ前記巻回方向に沿った前記断面において、前記所定領域のみに前記引張応力が導入された、請求項1又は2に記載の巻鉄心。
- 請求項1又は2に記載の巻鉄心の製造方法であって、
鋼板を折り曲げ加工する工程と、
鋼板を切断する工程と、
折り曲げられ、且つ切断された前記鋼板を層状に積み重ね、巻回方向の端部同士を突き合わせて巻回形状に組み付ける工程と、
前記端部の近傍において、又は切断前の前記端部となる位置の近傍において、板厚方向に引張応力を導入する工程と、
を備える、巻鉄心の製造方法。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP24815632.5A EP4723148A1 (en) | 2023-05-31 | 2024-05-31 | Wound iron core and method for manufacturing same |
| JP2024553483A JP7636706B1 (ja) | 2023-05-31 | 2024-05-31 | 巻鉄心およびその製造方法 |
| CN202480033629.8A CN121195319A (zh) | 2023-05-31 | 2024-05-31 | 卷绕铁芯及其制造方法 |
| KR1020257038759A KR20250174965A (ko) | 2023-05-31 | 2024-05-31 | 권철심 및 그 제조 방법 |
| AU2024281976A AU2024281976A1 (en) | 2023-05-31 | 2024-05-31 | Wound iron core and method for manufacturing same |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023090265 | 2023-05-31 | ||
| JP2023-090265 | 2023-05-31 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2024248153A1 true WO2024248153A1 (ja) | 2024-12-05 |
Family
ID=93657629
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2024/020114 Ceased WO2024248153A1 (ja) | 2023-05-31 | 2024-05-31 | 巻鉄心およびその製造方法 |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP4723148A1 (ja) |
| JP (1) | JP7636706B1 (ja) |
| KR (1) | KR20250174965A (ja) |
| CN (1) | CN121195319A (ja) |
| AU (1) | AU2024281976A1 (ja) |
| TW (1) | TWI877020B (ja) |
| WO (1) | WO2024248153A1 (ja) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2008127632A (ja) | 2006-11-21 | 2008-06-05 | Nippon Steel Corp | 低鉄損一方向性電磁鋼板 |
| WO2022092096A1 (ja) * | 2020-10-26 | 2022-05-05 | 日本製鉄株式会社 | 巻鉄心、巻鉄心の製造方法及び巻鉄心製造装置 |
| JP2022078444A (ja) | 2020-11-13 | 2022-05-25 | Jfeスチール株式会社 | 巻鉄心 |
-
2024
- 2024-05-31 JP JP2024553483A patent/JP7636706B1/ja active Active
- 2024-05-31 WO PCT/JP2024/020114 patent/WO2024248153A1/ja not_active Ceased
- 2024-05-31 AU AU2024281976A patent/AU2024281976A1/en active Pending
- 2024-05-31 TW TW113120322A patent/TWI877020B/zh active
- 2024-05-31 CN CN202480033629.8A patent/CN121195319A/zh active Pending
- 2024-05-31 EP EP24815632.5A patent/EP4723148A1/en active Pending
- 2024-05-31 KR KR1020257038759A patent/KR20250174965A/ko active Pending
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2008127632A (ja) | 2006-11-21 | 2008-06-05 | Nippon Steel Corp | 低鉄損一方向性電磁鋼板 |
| WO2022092096A1 (ja) * | 2020-10-26 | 2022-05-05 | 日本製鉄株式会社 | 巻鉄心、巻鉄心の製造方法及び巻鉄心製造装置 |
| JP2022078444A (ja) | 2020-11-13 | 2022-05-25 | Jfeスチール株式会社 | 巻鉄心 |
Non-Patent Citations (1)
| Title |
|---|
| TRANSACTIONS OF THE JAPAN SOCIETY OF MECHANICAL ENGINEERS, vol. 71, no. 711, 2005, pages 1530 |
Also Published As
| Publication number | Publication date |
|---|---|
| KR20250174965A (ko) | 2025-12-15 |
| EP4723148A1 (en) | 2026-04-08 |
| AU2024281976A1 (en) | 2025-12-18 |
| JP7636706B1 (ja) | 2025-02-27 |
| TW202503791A (zh) | 2025-01-16 |
| TWI877020B (zh) | 2025-03-11 |
| CN121195319A (zh) | 2025-12-23 |
| JPWO2024248153A1 (ja) | 2024-12-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6776952B2 (ja) | 巻鉄心 | |
| TWI773567B (zh) | 捲鐵心、捲鐵心之製造方法及捲鐵心製造裝置 | |
| JP7538440B2 (ja) | 巻鉄心 | |
| JP7107470B1 (ja) | 巻鉄心、巻鉄心の製造方法及び巻鉄心製造装置 | |
| WO2023058655A1 (ja) | 巻鉄心 | |
| JP7636706B1 (ja) | 巻鉄心およびその製造方法 | |
| JP7636705B1 (ja) | 巻鉄心およびその製造方法 | |
| CN116508120A (zh) | 卷绕铁芯 | |
| JP7695547B2 (ja) | 巻鉄心及び巻鉄心の製造方法 | |
| JP7541251B2 (ja) | 巻鉄心 | |
| JP7188662B2 (ja) | 巻鉄心 | |
| JP7648871B2 (ja) | 巻鉄心 | |
| JP7695546B2 (ja) | 巻鉄心 | |
| JP7680675B2 (ja) | 巻鉄心の製造方法及び製造装置 | |
| JP7601299B1 (ja) | 変圧器用鉄心および変圧器 | |
| WO2025254212A1 (ja) | 方向性電磁鋼板および巻鉄心 | |
| JP4276618B2 (ja) | 低鉄損一方向性電磁鋼板 | |
| JP4437939B2 (ja) | 低鉄損一方向性電磁鋼板 | |
| TW202601695A (zh) | 捲鐵心及其製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024553483 Country of ref document: JP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 24815632 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 1020257038759 Country of ref document: KR Free format text: ST27 STATUS EVENT CODE: A-0-1-A10-A15-NAP-PA0105 (AS PROVIDED BY THE NATIONAL OFFICE) |
|
| WWE | Wipo information: entry into national phase |
Ref document number: KR1020257038759 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: AU2024281976 Country of ref document: AU Ref document number: 202517118813 Country of ref document: IN |
|
| REG | Reference to national code |
Ref country code: BR Ref legal event code: B01A Ref document number: 112025025972 Country of ref document: BR |
|
| ENP | Entry into the national phase |
Ref document number: 2024281976 Country of ref document: AU Date of ref document: 20240531 Kind code of ref document: A |
|
| WWP | Wipo information: published in national office |
Ref document number: 202517118813 Country of ref document: IN |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024815632 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2025133147 Country of ref document: RU |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| ENP | Entry into the national phase |
Ref document number: 2024815632 Country of ref document: EP Effective date: 20260102 |
|
| WWP | Wipo information: published in national office |
Ref document number: 2025133147 Country of ref document: RU |
|
| WWP | Wipo information: published in national office |
Ref document number: 2024815632 Country of ref document: EP |