WO2014104983A1 - Process and apparatus for measuring of thickness of a probe during a tension test - Google Patents
Process and apparatus for measuring of thickness of a probe during a tension test Download PDFInfo
- Publication number
- WO2014104983A1 WO2014104983A1 PCT/SI2012/000067 SI2012000067W WO2014104983A1 WO 2014104983 A1 WO2014104983 A1 WO 2014104983A1 SI 2012000067 W SI2012000067 W SI 2012000067W WO 2014104983 A1 WO2014104983 A1 WO 2014104983A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- probe
- matrix
- thickness
- values
- pix
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B11/00—Measuring arrangements characterised by the use of optical techniques
- G01B11/16—Measuring arrangements characterised by the use of optical techniques for measuring the deformation in a solid, e.g. optical strain gauge
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N3/00—Investigating strength properties of solid materials by application of mechanical stress
- G01N3/02—Details
- G01N3/06—Special adaptations of indicating or recording means
- G01N3/068—Special adaptations of indicating or recording means with optical indicating or recording means
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N3/00—Investigating strength properties of solid materials by application of mechanical stress
- G01N3/08—Investigating strength properties of solid materials by application of mechanical stress by applying steady tensile or compressive forces
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N2203/00—Investigating strength properties of solid materials by application of mechanical stress
- G01N2203/02—Details not specific for a particular testing method
- G01N2203/06—Indicating or recording means; Sensing means
- G01N2203/0641—Indicating or recording means; Sensing means using optical, X-ray, ultraviolet, infrared or similar detectors
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N2203/00—Investigating strength properties of solid materials by application of mechanical stress
- G01N2203/02—Details not specific for a particular testing method
- G01N2203/06—Indicating or recording means; Sensing means
- G01N2203/0641—Indicating or recording means; Sensing means using optical, X-ray, ultraviolet, infrared or similar detectors
- G01N2203/0647—Image analysis
Definitions
- the present invention refers to a process and apparatus for measuring of thickness of a probe during a tension test.
- the aim of the invention is to enable accurate and reliable measuring of thickness of a probe during a tensioning test at least in the location of minimal cross-section of said probe.
- a tension test as such is intended for the purposes of determining and/or examining of physical properties of materials, in particular tensile strength, upper elastic limit, contraction or the like.
- a probe consisting of a known material and hawing known and standardized dimensions is fastened within a tension testing apparatus having a fixed jaw and a displaceable jaw, in which said probe is fastened.
- Said displaceable jaw can be displaced apart from said fixed jaw, by which the probe is tensioned.
- the tension force acting to the probe is permanently measured as well as deformation thereof, in particular strain and contraction.
- One of known methods for measuring thickness of the probe provides measuring of a diameter of the probe by means of suitable measuring instrument prior to performing the test, upon which the probe is tensioned and the diameter of such deformed probe is measured. On such basis, conclusions are then made about changing of the thickness during the test, which is not really reliable, in particular since also the thickness prior to testing and after that can actually be measured on different locations along the probe. Moreover, results of such measuring are not automatically and independently collected, which reduces accuracy of such measuring.
- a further approach provides use of two laser beams, which are directed towards each other and perpendicularly with respect to the longitudinal axis of the probe, which is then exposed to said beams in two points located in the diametrical plane thereof.
- the probe is tensioned, it is also extended, and both points, which are initially exposed to said beams, are displaced along such extending probe. Consequently, such measuring us also not performed always in the same location on the probe, since the measuring location is permanently displaced along the probe during the test, which systematically introduces certain discrepancies into said measuring, and such obtained results are never quite reliable.
- the third approach provides monitoring of the thickness by means of two video cameras, and change of thickness of the probe is permanently monitored and calculated by means of triangulation.
- two cameras, two supporting stands and other required equipment leads to essentially complicated concept of the measuring apparatus as such, which essentially increases the price and also the risk of malfunction.
- the initially raised problem is solved by means of features of a measuring apparatus as well as of process, which are included in independent patent claims including the embodiments according to dependent claims.
- Fig. 1 is a schematically presented perspective view of an apparatus for measuring of thickness of a probe according to the invention.
- Fig. 2 is a probe, which is suitable for such measuring.
- the present invention refers to an apparatus for measuring of thickness of a probe 2 during a tension test, wherein such apparatus comprises a tension testing device 1 with a fixed jaw 1 1 and a movable jaw 12, which are arranged above each other and adapted to hold each disposable standardized probe 2 having a measuring area defined by means of a diameter D mm and the length L mm , such that the longitudinal axis 20 of the probe 2 extends at least approximately in the vertical direction.
- the apparatus further comprises a video camera 3, which is adapted for monitoring the probe 2 during tensioning thereof and is arranged in the area of the tensioning device 1 appropriately apart from the probe 2, such that the optical axis 30 of the camera 3 is directed towards the longitudinal axis 20 of the probe 2 and perpendicularly with respect to said longitudinal axis 20 of the probe 2.
- said video camera 3 is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data interconnectable with a corresponding computer 4, which is adapted to receive, store, process and optionally also to display and/or to export the data received from the side of the previously mentioned video camera 3.
- the apparatus comprises a screen 5, which is suitable to provide contrast relative to the probe 2 and is arranged in the area of said tensioning apparatus 1 adjacent to the probe 2 and at appropriate distance apart from it, namely diametrically opposite to the video camera 3 with respect to the longitudinal axis 20 of the probe 2, wherein said screen 5 is intended to provide a contrast background behind the probe 2, when recorded by means of video camera 3 and is appropriately colored relative to each disposable surface of each corresponding probe 2.
- the apparatus according to the invention is furnished with a computer 4, which is suitable for cooperating with said video camera 3 and is adapted for
- - n is a number of columns of the input picture; ii) calculating average value x of pixels e.g. in a row corresponding to integer of m/2 according to the formula (I)
- D P ix 2 - i (IV); v) determining the length Z pix , along which said measuring of reduction of the thickness of the probe 2 is performed, wherein the ratio of original values of the diameter and the measuring length of the probe 2 according to formula (V) is calculated
- the computer 4 is further adapted to eliminate each errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix DD pix are taken into consideration by calculating thickness of the probe 2, wherein i) a histogram is created with such number of intervals, which corresponds to L pix - 1 , while two abscise axis values of the histogram correspond to minimum and maximum value of the matrix DD plx , by which a further matrix G is created with the size L pix - 1, in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is G max , upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function"; ii) all values of the matrix G, are reviewed by means of the "for loop
- the computer 4 is further adapted for calculating average thickness D A VG of the probe 2 in accordance with formula (VII):
- the computer 4 is further adapted for determining the thickness D AVG of the probe 2 as the minimum value of the matrix G zaJzracun .
- Apparatus according to the invention further comprises a bright, in particular white colored screen 5, while the probe 2 is darkened on its surface, in particular in the area of its diametrical plane, which extends throughout the longitudinal axis 20 of the probe 2 and at the same time also perpendicularly with respect to the optical axis 30 of the video camera 3.
- the invention further refers to a process for measuring of thickness of a probe 2 during a tension test, wherein each disposable standardized probe 2 having a measuring area defined by means of a diameter D mm and the length L mm is fastened into a tension testing device 1 furnished with at least one fixed jaw 1 1 and a movable jaw 12, which are arranged above each other and adapted to hold said probe 2, such that the longitudinal axis 20 of the probe 2 extends at least approximately in the vertical direction, and wherein said probe 2 in such fastened state and during tensioning thereof is recorded by means of a video camera 3, which is arranged in the area of the tensioning device 1 at appropriate distance apart from the probe 2, such that the optical axis 30 of the camera 3 is directed towards the longitudinal axis 20 of the probe 2 and perpendicularly with respect to said longitudinal axis 20 of the probe 2, and in addition to that, said video camera 3 is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data
- the process according to the invention provides that prior to recording by said video camera 3 a screen 5 is arranged adjacent to said probe 2, which is suitable to provide a contrast relative to the probe 2 and is arranged in the area of said tensioning device 1 adjacent to the probe 2 and at appropriate distance apart from it, namely diametrically opposite to the video camera 3 with respect to the longitudinal axis of the probe 2, wherein said screen 5 is intended to provide a contrast background behind the probe 2 during recording by means of video camera 3 and is appropriately colored relative to each disposable surface of each corresponding probe 2.
- the invention provides that the computer 4 cooperating with said video camera 3 is further adapted for i) converging each particular input picture of the measuring area L of the probe 2 as received from the video camera 3, from the " peg i.e. 24- byte RGB format into a matrix A consisting of 8-byte digits with values 0- 256 corresponding to each particular points i.e. pixels, wherein the dimensions of said matrix A are m x «, and wherein
- - n is a number of columns of the input picture; calculating an average value x of pixels e.g. in a row corresponding :ger of m/2 according to the formula (I)
- the value XQ corresponds to a value in the line and the column j in said matrix
- the average value x corresponds to the average values in the row ; iii) comparing each disposable values of pixels, wherein in the row
- a ⁇ x j 0 ⁇ n ⁇ x; B ⁇ [ ⁇ j-l, j ⁇ , ⁇ x , Xj ⁇ ],
- xi (* - «,)/* ! (Ill) upon which analogously also the value x 2 of the second line is determined, and the thickness of the probe 2 in pixels is calculated by means of formula (IV) on the basis of the difference v) determining the length Z, pix , along which said measuring of reduction of the thickness of the probe 2 is performed, wherein the ratio of original values of the diameter D mm and the measuring length L mm of the probe 2 according to formula ( V) is calculated
- R D nm /L mm (V) and the length L pix in pixels is determined by means of formula (VI) on the basis of thickness D pix in pixels and the previously mentioned ratio R
- L pix D p R (VI), by means of which for the purposes of further measuring of the thickness of the probe 2 then a sub-matrix W of size L pix x n is created, wherein the first row of said sub-matrix is the row numbered (m - L pix )/2 of the original matrix A, and the step of determining the thickness of the probe 2 is then repeated in each row of said sub-matrix W, so that in each row of the sub- matrix W the thickness Z> pix of the probe 2 in pixels is determined, and for each image generated by means of the video camera 3 then a matrix DD pix of size Xpj x x 1 is created.
- the computer 4 is further used for the purposes of eliminating errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix DD pix are taken into consideration by calculating thickness of the probe 2, wherein i) a histogram is created with such number of intervals, which corresponds to L pix - 1 , while two abscise axis values of the histogram correspond to minimum and maximum value of the matrix DD pix , by which a further matrix G is created with the size L p j x - 1 , in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is G max , upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function";
- an average thickness D AVG of the probe 2 is determined in accordance with formula (VII):
- each thickness of the probe 2 is determined on the basis of the minimum value of the matrix (G za _ izracun ).
- each particular scalar value of each particular image is transformed into a matrix of values of the thickness D jzrac , on the basis of which then also a contraction can be calculated by means of Formula ( VIII)
- the apparatus and process according to the invention enable permanent monitoring of the thickness of the probe 2 on the same location on the probe 2 during the tension test, when the probe 2 is fastened within the tension testing device 1 and exposed to each known and measured force, and also to calculate a relative contraction and other physical properties of the material of the probe 2. All the data is permanently and independently recorded, and such retrieved data about identified changes during the whole testing up to destruction of the probe 2 can later serve as an input data for the purposes of simulating various loading examples in the finite element analysis, by which stresses and deformations in mechanically loaded parts can be foreseen not only in the area of elastic deformations but also in the area of plastic deformations.
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Health & Medical Sciences (AREA)
- Life Sciences & Earth Sciences (AREA)
- Chemical & Material Sciences (AREA)
- Analytical Chemistry (AREA)
- Biochemistry (AREA)
- General Health & Medical Sciences (AREA)
- Immunology (AREA)
- Pathology (AREA)
- Investigating Strength Of Materials By Application Of Mechanical Stress (AREA)
- Length Measuring Devices By Optical Means (AREA)
Abstract
Apparatus for measuring of thickness of a probe (2) during a tension test comprises a tensioning device (1), which is furnished with a fixed jaw (11) and a displaceable jaw (12), which are arranged above each other and are adapted for clamping and tensioning of each disposable standardized probe (2), as well as a video camera (3), which is arranged in the area of said tensioning device (1) at appropriate distance apart of the probe (2), so that the optical axis (30) of the video camera (3) extends towards the longitudinal axis (20) of the probe (2) and rectangular with respect to said longitudinal axis (20) of the probe (2). The apparatus further comprises a screen (5), which forms a contrast background behind the probe (2) and is with respect to said video camera (3) arranged on the opposite side of the probe (2), and moreover also a computer (4), which is adapted for retrieving, saving and processing of data received from the video camera (3).
Description
PROCESS AND APPARATUS FOR MEASURING OF THICKNESS OF A PROBE DURING A TENSION TEST
The present invention refers to a process and apparatus for measuring of thickness of a probe during a tension test.
The aim of the invention is to enable accurate and reliable measuring of thickness of a probe during a tensioning test at least in the location of minimal cross-section of said probe.
A tension test as such is intended for the purposes of determining and/or examining of physical properties of materials, in particular tensile strength, upper elastic limit, contraction or the like. In this, a probe consisting of a known material and hawing known and standardized dimensions is fastened within a tension testing apparatus having a fixed jaw and a displaceable jaw, in which said probe is fastened. Said displaceable jaw can be displaced apart from said fixed jaw, by which the probe is tensioned. During said tension test, the tension force acting to the probe is permanently measured as well as deformation thereof, in particular strain and contraction.
One of known methods for measuring thickness of the probe provides measuring of a diameter of the probe by means of suitable measuring instrument prior to performing the test, upon which the probe is tensioned and the diameter of such deformed probe is measured. On such basis, conclusions are then made about changing of the thickness during the test, which is not really reliable, in particular since also the thickness prior to testing and after that can actually be measured on different locations along the probe. Moreover, results of such measuring are not automatically and independently collected, which reduces accuracy of such measuring.
A further approach provides use of two laser beams, which are directed towards each other and perpendicularly with respect to the longitudinal axis of the probe, which is then exposed to said beams in two points located in the diametrical plane thereof. When the probe is tensioned, it is also extended, and both points, which are initially exposed to said beams, are displaced along such extending probe. Consequently, such measuring us also not performed always in the same location on the probe, since the measuring location is permanently displaced along the probe during the test, which systematically introduces certain discrepancies into said measuring, and such obtained results are never quite reliable.
The third approach provides monitoring of the thickness by means of two video cameras, and change of thickness of the probe is permanently monitored and calculated by means of triangulation. However, such application of two cameras, two supporting stands and other required equipment leads to essentially complicated concept of the measuring apparatus as such, which essentially increases the price and also the risk of malfunction.
According to the invention, the initially raised problem is solved by means of features of a measuring apparatus as well as of process, which are included in independent patent claims including the embodiments according to dependent claims.
The invention will be described on the basis of an embodiment, which is presented in the attached drawings, wherein
Fig. 1 is a schematically presented perspective view of an apparatus for measuring of thickness of a probe according to the invention; and
Fig. 2 is a probe, which is suitable for such measuring.
The present invention refers to an apparatus for measuring of thickness of a probe 2 during a tension test, wherein such apparatus comprises a tension testing device 1 with a fixed jaw 1 1 and a movable jaw 12, which are arranged above each other and adapted to hold each disposable standardized probe 2 having a measuring area defined by means of a diameter Dmm and the length Lmm, such that the longitudinal axis 20 of the probe 2 extends at least approximately in the vertical direction. The apparatus further comprises a video camera 3, which is adapted for monitoring the probe 2 during tensioning thereof and is arranged in the area of the tensioning device 1 appropriately apart from the probe 2, such that the optical axis 30 of the camera 3 is directed towards the longitudinal axis 20 of the probe 2 and perpendicularly with respect to said longitudinal axis 20 of the probe 2. In addition, said video camera 3 is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data interconnectable with a corresponding computer 4, which is adapted to receive, store, process and optionally also to display and/or to export the data received from the side of the previously mentioned video camera 3.
The invention provides that the apparatus comprises a screen 5, which is suitable to provide contrast relative to the probe 2 and is arranged in the area of said tensioning apparatus 1 adjacent to the probe 2 and at appropriate distance apart from it, namely diametrically opposite to the video camera 3 with respect to the longitudinal axis 20 of the probe 2, wherein said screen 5 is intended to provide a contrast background behind the probe 2, when recorded by means of video camera 3 and is appropriately colored relative to each disposable surface of each corresponding probe 2.
Moreover, the apparatus according to the invention is furnished with a computer 4, which is suitable for cooperating with said video camera 3 and is adapted for
i) converging each particular input picture of the measuring area L of the probe 2 as received from the video camera 3, from the " peg" i.e. 24- byte RGB format into a matrix A consisting of 8-byte digits with values 0- 256 corresponding to each particular points i.e. pixels, wherein the dimensions of said matrix A are m x n, and wherein
- m is a number of rows of the input picture; and
- n is a number of columns of the input picture; ii) calculating average value x of pixels e.g. in a row corresponding to integer of m/2 according to the formula (I)

(I)
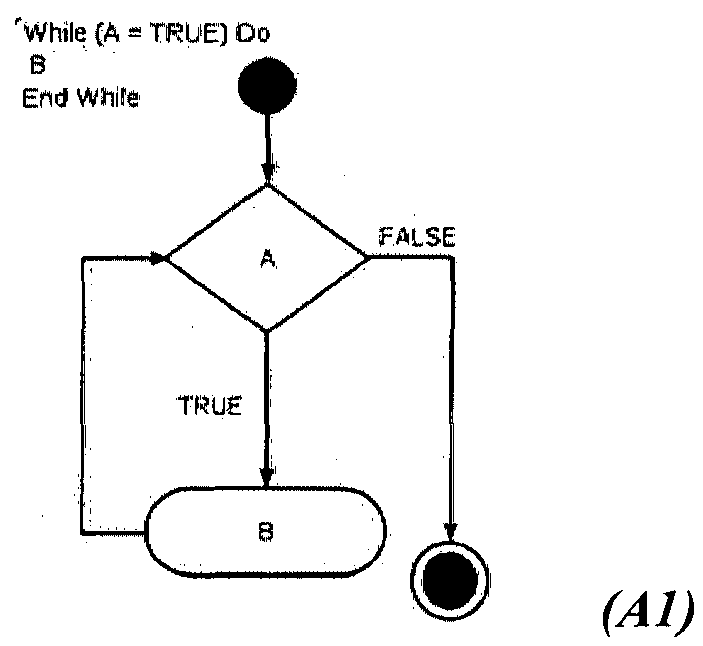
wherein the value xtj corresponds to a value in the line and the column j in said matrix, and the average value x corresponds to the average values in the row ; iii) comparing each disposable values of pixels, wherein in the row |m 2 such location i.e. such value j of the first and the last value in the row is determined, which is smaller than the average value x, as well as the location of two neighboring values, which are not yet larger than the calculated average value, which is performed according to algorithm Al
"While (A = TRUE) Do

wherein the result of the first transition is
A→ Xj=o→n < S B → [{j-l, j}, {Xj. Xj }] ,
and the result of the last transition is
A→xj=n→o < x; B → [{j, j+1 }, {xs, xi+i } ] ; iv) determining borders as well as the thickness of the probe 2 on the basis of calculation of a pair of lines, which are each per se extending through two points from each particular matrix, wherein a pair of values x is calculated, in which said lines correspond to previously calculated average value x,
wherein the general formula (II) of each line is y = k x x + n, (II) where k is a coefficient of inclination, and n is a section on the ordinate axis, so that the first line with the inclination coefficient kj and the section «7 on the ordinate axis is calculated by means of points T](j-1, Χ ) and T2 j, Xj), by which it is calculated, in which point xt the line corresponds to the value, which is equal to previously calculated average value according to formula (III)
xx = (x - nx)lkx (III) upon which analogously also the value x2 of the second line is determined, and the thickness of the probe 2 in pixels is calculated by means of formula (IV) on the basis of the difference
DPix = 2 - i (IV); v) determining the length Zpix, along which said measuring of reduction of the thickness of the probe 2 is performed, wherein the ratio of original values of the diameter and the measuring length of the probe 2 according to formula (V) is calculated
R = Dmm/Lmm (V) and the length Z,pix in pixels is determined by means of formula (VI) on the basis of thickness Dpix in pixels and the previously mentioned ratio R
Lpix = Dpix/R (VI), by means of which for the purposes of further measuring of the thickness of the probe 2 then a sub-matrix W of size LpiX x n is created, wherein the first row of said sub-matrix is the row numbered (m - Lpix)/2 of the original matrix A, and the step of determining the thickness of the probe 2 is then repeated in each row of said sub-matrix W, so that in each row of the sub- matrix W the thickness Dpix of the probe 2 in pixels is determined, and for each image generated by means of the video camera 3 then a matrix DDpix of size LpiX x 1 is created.
In accordance with a preferred embodiment of the invention, the computer 4 is further adapted to eliminate each errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix DDpix are taken into consideration by calculating thickness of the probe 2, wherein i) a histogram is created with such number of intervals, which corresponds to Lpix - 1 , while two abscise axis values of the histogram correspond to minimum and maximum value of the matrix DDplx, by which a further matrix G is created with the size Lpix - 1, in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is Gmax, upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function";
ii) all values of the matrix G, are reviewed by means of the "for loop", and for each particular value between Gmax/6 in 5 x Gmax/6, the value from the first column of the matrix G is inserted into a newly created matrix Goph in which all indexes are considered, in which the measuring results of the matrix G are taken into consideration, upon which a further matrix Gza izracun is created of size (2 x LpjX/3) x 1, in which all values from the second column of each particular indexes in the matrix G are present, which are included within the matrix Gopt.
In accordance with a further aspect of the invention, the computer 4 is further adapted for calculating average thickness DA VG of the probe 2 in accordance with formula (VII):

In accordance with a still further aspect of the invention, the computer 4 is further adapted for determining the thickness DAVG of the probe 2 as the minimum value of the matrix GzaJzracun.
Apparatus according to the invention further comprises a bright, in particular white colored screen 5, while the probe 2 is darkened on its surface, in particular in the area of its diametrical plane, which extends throughout the longitudinal axis 20 of the probe 2 and at the same time also perpendicularly with respect to the optical axis 30 of the video camera 3.
The invention further refers to a process for measuring of thickness of a probe 2 during a tension test, wherein each disposable standardized probe 2 having a measuring area defined by means of a diameter Dmm and the length Lmm is fastened into a tension testing device 1 furnished with at least one fixed jaw 1 1 and a movable jaw 12, which are arranged above each other and adapted to hold said probe 2, such that the longitudinal axis 20 of the probe 2 extends at least approximately in the vertical direction, and wherein said probe 2 in such fastened state and during tensioning thereof is recorded by means of a video camera 3, which is arranged in the area of the tensioning device 1 at appropriate distance apart from the probe 2, such that the optical axis 30 of the camera 3 is directed towards the longitudinal axis 20 of the probe 2 and perpendicularly with respect to said longitudinal axis 20 of the probe 2, and in addition to that, said video camera 3 is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data interconnectable with a corresponding computer 4, which is adapted to receive, store, process and optionally also to display and/or to export the data received from the side of the previously mentioned video camera 3.
The process according to the invention provides that prior to recording by said video camera 3 a screen 5 is arranged adjacent to said probe 2, which is suitable to provide a contrast relative to the probe 2 and is arranged in the area of said tensioning device 1 adjacent to the probe 2 and at appropriate distance apart from it, namely diametrically opposite to the video camera 3 with respect to the longitudinal axis of the probe 2, wherein said screen 5 is intended to provide a contrast background behind the probe 2 during recording by means of video camera 3 and is appropriately colored relative to each disposable surface of each corresponding probe 2.
Besides, the invention provides that the computer 4 cooperating with said video camera 3 is further adapted for i) converging each particular input picture of the measuring area L of the probe 2 as received from the video camera 3, from the " peg i.e. 24- byte RGB format into a matrix A consisting of 8-byte digits with values 0- 256 corresponding to each particular points i.e. pixels, wherein the dimensions of said matrix A are m x «, and wherein
- m is a number of rows of the input picture; and
- n is a number of columns of the input picture; calculating an average value x of pixels e.g. in a row corresponding :ger of m/2 according to the formula (I)

wherein the result of the first transition is
A→xj=0→n < x; B → [{j-l, j}, {x , Xj } ],
and the result of the last transition is
A→ Xj=n→o < ; B → {J¾, xj+1 }]; iv) determining borders as well as the thickness of the probe 2 on the basis of calculation of a pair of lines, which are each per se extending through two points from each particular matrix, wherein a pair of values x is calculated , in which said lines correspond to previously calculated average value x, wherein the general formula (II) of each line is y = k x x + n, (Π) where k is a coefficient of inclination, and n is a section on the ordinate axis, so that the first line with the inclination coefficient kj and the section «7 on the ordinate axis is calculated by means of points Ti (j-1, xj.j) and T2 j, Xj), by which it is calculated, in which point i the line corresponds to the
value, which is equal to previously calculated average value according to formula (III)
xi = (* - «,)/*! (Ill) upon which analogously also the value x2 of the second line is determined, and the thickness of the probe 2 in pixels is calculated by means of formula (IV) on the basis of the difference
 v) determining the length Z,pix, along which said measuring of reduction of the thickness of the probe 2 is performed, wherein the ratio of original values of the diameter Dmm and the measuring length Lmm of the probe 2 according to formula ( V) is calculated
R = Dnm/Lmm (V) and the length Lpix in pixels is determined by means of formula (VI) on the basis of thickness Dpix in pixels and the previously mentioned ratio R
Lpix = Dp R (VI), by means of which for the purposes of further measuring of the thickness of the probe 2 then a sub-matrix W of size Lpix x n is created, wherein the first row of said sub-matrix is the row numbered (m - Lpix)/2 of the original matrix A, and the step of determining the thickness of the probe 2 is then repeated in each row of said sub-matrix W, so that in each row of the sub-
matrix W the thickness Z>pix of the probe 2 in pixels is determined, and for each image generated by means of the video camera 3 then a matrix DDpix of size Xpjx x 1 is created.
In a preferred embodiment of the process according to the invention, the computer 4 is further used for the purposes of eliminating errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix DDpix are taken into consideration by calculating thickness of the probe 2, wherein i) a histogram is created with such number of intervals, which corresponds to Lpix - 1 , while two abscise axis values of the histogram correspond to minimum and maximum value of the matrix DDpix, by which a further matrix G is created with the size Lpjx - 1 , in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is Gmax, upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function";
ii) all values of the matrix G, are reviewed by means of the "for loop", and for each particular value between Gmax/6 in 5 χ Gmax/6, the value from the first column of the matrix G is inserted into a newly created matrix Gopt, in which all indexes are considered, in which the measuring results of the matrix G are taken into consideration, upon which a further matrix Gza izracun is created of size (2 x Lpjx/3) x 1, in which all values from the second column of each particular indexes in the matrix G are present, which are included within the matrix Gopt.
In accordance with a further aspect of the invention, an average thickness DAVG of the probe 2 is determined in accordance with formula (VII):
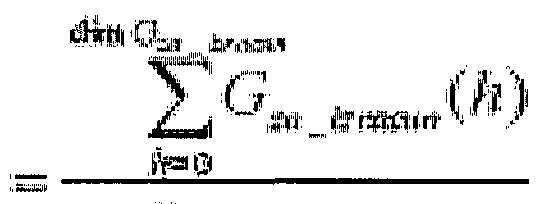
In accordance with a still further aspect of the invention, each thickness of the probe 2 is determined on the basis of the minimum value of the matrix (Gza_izracun).
When desired, each particular scalar value of each particular image is transformed into a matrix of values of the thickness Djzrac, on the basis of which then also a contraction can be calculated by means of Formula ( VIII)
D% = 100 x [1 - Dizrac(k)/Dizrac (0)] (VIII)
The apparatus and process according to the invention enable permanent monitoring of the thickness of the probe 2 on the same location on the probe 2 during the tension test, when the probe 2 is fastened within the tension testing device 1 and exposed to each known and measured force, and also to calculate a relative contraction and other physical properties of the material of the probe 2. All the data is permanently and independently recorded, and such retrieved data about identified changes during the whole testing up to destruction of the probe 2 can later serve as an input data for the purposes of simulating various loading examples in the finite element analysis, by which stresses and deformations in mechanically loaded parts can be foreseen not only in the area of elastic deformations but also in the area of plastic deformations.
Claims
PATENT CLAIMS
1. Apparatus for measuring of thickness of a probe (2) during a tension test, comprising a tension testing device (1) with a fixed jaw (1 1) and a movable jaw (12), which are arranged above each other and adapted to hold each disposable standardized probe (2) having a measuring area defined by means of a diameter (Dmm) and the length (Lmm), such that the longitudinal axis (20) of the probe (2) extends at least approximately in the vertical direction, as well as a video camera (3), which is adapted for monitoring the probe (2) during tensioning thereof and is arranged in the area of the tensioning device (1) appropriately apart from the probe
(2) , such that the optical axis (30) of the camera (3) is directed towards the longitudinal axis (20) of the probe (2) and perpendicularly with respect to said longitudinal axis (20) of the probe (2), and in addition to that, said video camera
(3) is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data interconnectable with a corresponding computer (4), which is adapted to receive, store, process and optionally also to display and/or to export the data received from the side of the previously mentioned video camera (3), characterized in that the apparatus comprises a screen (5), which is suitable to provide contrast relative to the probe (2) and is arranged in the area of said tensioning device (1) adjacent to the probe (2) and at appropriate distance apart from it, namely diametrically opposite to the video camera (3) with respect to the longitudinal axis (20) of the probe (2), wherein said screen (5) is intended to provide a contrast background behind the probe (2) when recorded by means of video camera (3) and is appropriately colored relative to each disposable surface of each corresponding probe (2), and in that the computer (4) cooperating with said video camera (3) is adapted for
i) converging each particular input picture of the measuring area (L) of the probe (2) as received from the video camera (3), from the "j eg^' i.e. 24-byte RGB format into a matrix (A) consisting of 8-byte digits with values 0-256 corresponding to each particular points i.e. pixels, wherein the dimensions of said matrix (A) are nt ft, and wherein
- m is a number of rows of the input picture; and
- n is a number of columns of the input picture; ii) calculating average value (x) of pixels e.g. in a row corresponding to integer of m/2 according to the formula (I)


wherein the result of the first transition is
A→ Xj=0→n < X; B → [{j-l, j}, {XjA , X} } ] ,
and the result of the last transition is
A→xj=n→o < x; B → iv) determining borders as well as the thickness of the probe (2) on the basis of calculation of a pair of lines, which are each per se extending through two points from each particular matrix, wherein a pair of values (x) is calculated, in which said lines correspond to previously calculated average value (X"), wherein the general formula (II) of each line is y = k x x + n, (II) where k is a coefficient of inclination, and n is a section on the ordinate axis, so that the first line with the inclination coefficient (kj) and the section on the ordinate axis is calculated by means of points Ti(j-1 , XJ. J) and T2(j, Xj), by which it is calculated, in which point (xi) the line corresponds
to the value, which is equal to previously calculated average value according to formula (III)
x = (x - nx)lkx (III) upon which analogously also the value (x2) of the second line is determined, and the thickness of the probe (2) in pixels is calculated by means of formula (IV) on the basis of the difference
Opix = x2 - xi (IV); v) determining the length (Lpix), along which said measuring of reduction of the thickness of the probe (2) is performed, wherein the ratio of original values of the diameter (Z mm) and the measuring length (Z,mm) of the probe (2) according to formula (V) is calculated
R = Dm Lmm (V) and the length (Lpix) in pixels is determined by means of formula ( VI) on the basis of thickness (Dplx) in pixels and the previously mentioned ratio (if)
Lpix = Dpix/R (VI), by means of which for the purposes of further measuring of the thickness of the probe (2) then a sub-matrix (W) of size Lpix x n is created, wherein the first row of said sub-matrix is the row numbered (m - Lpix)/2 of the original matrix (^4), and the step of determining the thickness of the probe (2) is then repeated in each row of said sub-matrix (W), so that in each row of the sub-
matrix (W) the thickness (Z)pix) of the probe (2) in pixels is determined, and for each image generated by means of the video camera (3) then a matrix (Z)Z) pix) of size Z,pjx x 1 is created.
2. Apparatus according to Claim 1, characterized in that the computer (4) is further adapted to eliminate each errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix (DDpix) are taken into consideration by calculating thickness of the probe (2), wherein i) a histogram is created with such number of intervals, which corresponds to Lpix - 1, while two abscise axis values of the histogram correspond to minimum and maximum value of the matrix (DDpix), by which a further matrix (<7) is created with the size LPjx - 1 , in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is Gmax, upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function";
ii) all values of the matrix (G), are reviewed by means of the "for loop", and for each particular value between Gmax/6 in 5 x Gmax/6, the value from the first column of the matrix (G) is inserted into a newly created matrix (Gopt), in which all indexes are considered, in which the measurung results of the matrix (G) are taken into consideration, upon which a further matrix (Gzajzracun) is created of size (2 LpjX/3) x 1, in which all values from the second column of each particular indexes in the matrix G) are present, which are included within the matrix (Gopt).
3. Apparatus according to Claim 2, characterized in that the computer (4) is further adapted for calculating average thickness (DAVG) of the probe (2) in accordance with formula
 ( vii).
4. Apparatus according to Claim 2, characterized in that the computer (4) is further adapted for determining the thickness (DAVG) of the probe (2) as the minimum value of the matrix (Gzajzracun).
5. Apparatus according to anyone of Claims 1 - 4, characterized in that the contrast screen (5) is bright, in particular white colored, while the probe (2) is darkened on its surface, in particular in the area of its diametrical plane, which extends throughout the longitudinal axis (20) of the probe (2) and at the same time also perpendicularly with respect to the optical axis (30) of the video camera (3).
6. Process for measuring of thickness of a probe (2) during a tension test, wherein each disposable standardized probe (2) having a measuring area defined by means of a diameter (Dmm) and the length (Lmm) is fastened into a tension testing device (1) furnished with at least one fixed jaw (1 1) and a movable jaw (12), which are arranged above each other and adapted to hold said probe (2), such that the longitudinal axis (20) of the probe (2) extends at least approximately in the vertical direction, and wherein said probe (2) in such fastened state and during tensioning thereof is recorded by means of a video camera (3), which is arranged in the area of the tensioning device (1) at appropriate distance apart from the probe (2), such that the optical axis (30) of the camera (3) is directed towards the
longitudinal axis (20) of the probe (2) and perpendicularly with respect to said longitudinal axis (20) of the probe (2), and in addition to that, said video camera (3) is suitable for generating video recordings in the format "jpeg" i.e. 24-bit RGB format, and is optionally for the purposes of transmission of data interconnectable with a corresponding computer (4), which is adapted to receive, store, process and optionally also to display and/or to export the data received from the side of the previously mentioned video camera (3), characterized in that prior to recording by said video camera (3) a screen (5) is arranged adjacent to said probe (2), which is suitable to provide a contrast relative to the probe (2) and is arranged in the area of said tensioning device (1) adjacent to the probe (2) and at appropriate distance apart from it, namely diametrically opposite to the video camera (3) with respect to the longitudinal axis of the probe (2), wherein said screen (5) is intended to provide a contrast background behind the probe (2) during recording by means of video camera (3) and is appropriately colored relative to each disposable surface of each corresponding probe (2), and in that the computer (4) cooperating with said video camera (3) is adapted for i) converging each particular input picture of the measuring area (L) of the probe (2) as received from the video camera (3), from the "Jpeg" i.e. 24-byte RGB format into a matrix (A) consisting of 8-byte digits with values 0-256 corresponding to each particular points i.e. pixels, wherein the dimensions of said matrix (^4) are m x tt, and wherein
- m is a number of rows of the input picture; and
- n is a number of columns of the input picture; ii) calculating average value (x) of pixels e.g. in a row corresponding to integer oim/2 according to the formula (I)

n - I CO wherein the value X corresponds to a value in the line and the column j in said matrix, and the average value (x) corresponds to the average values in the row / iii) comparing each disposable values of pixels, wherein in the row |m/2 such location i.e. such value j of the first and the last value in the row is determined, which is smaller than the average value (5c), as well as the location of two neighboring values, which are not yet larger than the calculated average value, which is performed according to algorithm (Al)
'While (A " TRUE) Do

wherein the result of the first transition is
A→ Xj=0. •n < x; B [{j-l j}. {xj- Xj}] ,
and the result of the last transition is
A→ x ^j,=n→0 < x; B [{jj+i } , { j, j+i } ] ;
iv) determining borders as well as the thickness of the probe (2) on the basis of calculation of a pair of lines, which are each per se extending through two points from each particular matrix, wherein a pair of values (x) is calculated, in which said lines correspond to previously calculated average value ( ), wherein the general formula (II) of each line is y = k x x + n, (II) where (k) is a coefficient of inclination, and (n) is a section on the ordinate axis, so that the first line with the inclination coefficient (k ) and the section («/) on the ordinate axis is calculated by means of points ] (J- 1 , Xj.i) and T2(j, Xj), by which it is calculated, in which point (xi) the line corresponds to the value, which is equal to previously calculated average value according to formula (III)
X\ = (x - n\)lk\ (III) upon which analogously also the value (x2) of the second line is determined, and the thickness of the probe (2) in pixels is calculated by means of formula (IV) on the basis of the difference
 v) determining the length ( piX), along which said measuring of reduction of the thickness of the probe (2) is performed, wherein the ratio of
original values of the diameter (Dmm) and the measuring length (Lmm) of the probe (2) according to formula ( V) is calculated
R = Dm Lmm (V) and the length (Lpix) in pixels is determined by means of formula ( VI) on the basis of thickness (Dpix) in pixels and the previously mentioned ratio (R)
Lpix = Dpix/R (VI), by means of which for the purposes of further measuring of the thickness of the probe (2) then a sub-matrix (W) of size Lpix n is created, wherein the first row of said sub-matrix is the row numbered (m - Lpix)/2 of the original matrix (A), and the step of determining the thickness of the probe (2) is then repeated in each row of said sub-matrix (W), so that in each row of the sub- matrix (W) the thickness (Dpix) of the probe (2) in pixels is determined, and for each image generated by means of the video camera (3) then a matrix (DDpix) of size Lp x x 1 is created.
6. Process according to Claim 6, characterized in that the computer (4) is further used for the purposes of eliminating errors due to image noise, by anticipating that said error is statistically distributed in accordance with the Gauss distribution curve, and 2/3 of the matrix (DDpix) are taken into consideration by calculating thickness of the probe (2), wherein i) a histogram is created with such number of intervals, which corresponds to Lpix - 1, while two abscise axis values of the histogram
correspond to minimum and maximum value of the matrix (DDpix), by which a further matrix (G) is created with the size LPjX - 1 , in which the first column comprises values on the abscise axis of said histogram, and the second column comprises correlated values on the ordinate axis of said histogram, wherein the maximum value in said second column is Gmax, upon which the values in said second column are numerically integrated in order to obtain a curve similar to "error function"; ii) all values of the matrix (G), are reviewed by means of the "for loop", and for each particular value between Gmax/6 in 5 x Gmax/6, the value from the first column of the matrix (G) is inserted into a newly created matrix (Gopt), in which all indexes are considered, in which the measuring results of the matrix (G) are taken into consideration, upon which a further matrix (Gza zracun) is created of size (2 x Lp;x/3) x 1 , in which all values from the second column of each particular indexes in the matrix (G) are present, which are included within the matrix (Gopt).
8. Process according to Claim 7, characterized in that average thickness (DAVG) of the probe (2) is determined in accordance with formula (VII):

9. Process according to Claim 7, characterized in that thickness of the probe (2) is determined on the basis of the minimum value of the matrix (Gzajzracun).
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/SI2012/000067 WO2014104983A1 (en) | 2012-12-27 | 2012-12-27 | Process and apparatus for measuring of thickness of a probe during a tension test |
| PCT/SI2013/000087 WO2014104986A1 (en) | 2012-12-27 | 2013-12-23 | Video extensiometer |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/SI2012/000067 WO2014104983A1 (en) | 2012-12-27 | 2012-12-27 | Process and apparatus for measuring of thickness of a probe during a tension test |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2014104983A1 true WO2014104983A1 (en) | 2014-07-03 |
Family
ID=47884482
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/SI2012/000067 Ceased WO2014104983A1 (en) | 2012-12-27 | 2012-12-27 | Process and apparatus for measuring of thickness of a probe during a tension test |
| PCT/SI2013/000087 Ceased WO2014104986A1 (en) | 2012-12-27 | 2013-12-23 | Video extensiometer |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/SI2013/000087 Ceased WO2014104986A1 (en) | 2012-12-27 | 2013-12-23 | Video extensiometer |
Country Status (1)
| Country | Link |
|---|---|
| WO (2) | WO2014104983A1 (en) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104482840A (en) * | 2014-11-20 | 2015-04-01 | 航天海鹰(镇江)特种材料有限公司 | Force application device and detection method for detecting mold attaching gap of composite material wall plate |
| FR3093175A1 (en) * | 2019-02-21 | 2020-08-28 | Safran Aircraft Engines | SYSTEM FOR MEASURING BENDING SURFACE DEFORMATION OF A MATERIAL |
| WO2020263558A1 (en) * | 2019-06-25 | 2020-12-30 | Illinois Tool Works Inc. | Video extensometer system with reflective back screen |
| WO2020263559A1 (en) * | 2019-06-25 | 2020-12-30 | Illinois Tool Works Inc. | Brightness and contrast correction for video extensometer systems and methods |
| EP2990775B1 (en) * | 2014-08-28 | 2021-03-03 | The Boeing Company | Systems and methods for detecting crack growth |
| US20210404929A1 (en) * | 2020-06-29 | 2021-12-30 | Illinois Tool Works Inc. | Thickness correction for video extensometer systems and methods |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104330315A (en) * | 2014-11-06 | 2015-02-04 | 重庆戴卡捷力轮毂制造有限公司 | Device for rapidly measuring percentage elongation of tensile test bar |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5033096A (en) * | 1987-04-22 | 1991-07-16 | John Lysaght (Australia) Limited | Non-contact determination of the position of a rectilinear feature of an article |
| JP2000146787A (en) * | 1998-11-05 | 2000-05-26 | Nippon Steel Corp | Aperture measurement method for tensile test |
| US20030182069A1 (en) * | 2002-02-08 | 2003-09-25 | Banes Albert J. | Method and system for measuring properties of deformable material specimens |
-
2012
- 2012-12-27 WO PCT/SI2012/000067 patent/WO2014104983A1/en not_active Ceased
-
2013
- 2013-12-23 WO PCT/SI2013/000087 patent/WO2014104986A1/en not_active Ceased
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5033096A (en) * | 1987-04-22 | 1991-07-16 | John Lysaght (Australia) Limited | Non-contact determination of the position of a rectilinear feature of an article |
| JP2000146787A (en) * | 1998-11-05 | 2000-05-26 | Nippon Steel Corp | Aperture measurement method for tensile test |
| US20030182069A1 (en) * | 2002-02-08 | 2003-09-25 | Banes Albert J. | Method and system for measuring properties of deformable material specimens |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2990775B1 (en) * | 2014-08-28 | 2021-03-03 | The Boeing Company | Systems and methods for detecting crack growth |
| CN104482840A (en) * | 2014-11-20 | 2015-04-01 | 航天海鹰(镇江)特种材料有限公司 | Force application device and detection method for detecting mold attaching gap of composite material wall plate |
| FR3093175A1 (en) * | 2019-02-21 | 2020-08-28 | Safran Aircraft Engines | SYSTEM FOR MEASURING BENDING SURFACE DEFORMATION OF A MATERIAL |
| US11231265B2 (en) | 2019-02-21 | 2022-01-25 | Safran Aircraft Engines | System for measuring a bending deformation of a surface of a material |
| WO2020263559A1 (en) * | 2019-06-25 | 2020-12-30 | Illinois Tool Works Inc. | Brightness and contrast correction for video extensometer systems and methods |
| WO2020263558A1 (en) * | 2019-06-25 | 2020-12-30 | Illinois Tool Works Inc. | Video extensometer system with reflective back screen |
| CN114270813A (en) * | 2019-06-25 | 2022-04-01 | 伊利诺斯工具制品有限公司 | Video extensometer system with reflective rear screen |
| JP2022540778A (en) * | 2019-06-25 | 2022-09-20 | イリノイ トゥール ワークス インコーポレイティド | Brightness and Contrast Correction for Video Extensometer Systems and Methods |
| US11803943B2 (en) | 2019-06-25 | 2023-10-31 | Illinois Tool Works Inc. | Brightness and contrast correction for video extensometer systems and methods |
| JP7539934B2 (en) | 2019-06-25 | 2024-08-26 | イリノイ トゥール ワークス インコーポレイティド | Brightness and contrast correction for video extensometer systems and methods |
| US12254605B2 (en) | 2019-06-25 | 2025-03-18 | Illinois Tool Works Inc. | Systems for width measurement corrections of test specimens based on background brightness data of captured images |
| US20210404929A1 (en) * | 2020-06-29 | 2021-12-30 | Illinois Tool Works Inc. | Thickness correction for video extensometer systems and methods |
| US11867668B2 (en) * | 2020-06-29 | 2024-01-09 | Illinois Tool Works Inc. | Thickness correction for video extensometer systems and methods |
| US20240142355A1 (en) * | 2020-06-29 | 2024-05-02 | Illinois Tool Works Inc. | Thickness correction for video extensometer systems and methods |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2014104986A1 (en) | 2014-07-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111220463B (en) | A system and method for predicting uniaxial compressive strength of rock | |
| JP5343219B2 (en) | Strain measurement method, strain measurement system | |
| KR101094069B1 (en) | Calibration Device and Method for Correction of Threshold Value of Crack Measurement System Using Image Processing Technique | |
| JPWO2020065815A1 (en) | Material tester | |
| KR20160077704A (en) | Method of obtaining reliable true stress-strain curves in a large range of strains in tensile testing using digital image correlation | |
| WO2008073700A3 (en) | Method for assessing image focus quality | |
| CN104181030B (en) | Crop lodging resistance strength rapid tester | |
| KR101764640B1 (en) | image-based portable surface crack detecting apparatus | |
| WO2014104986A1 (en) | Video extensiometer | |
| JP7253284B2 (en) | STRESS AND STRAIN DISTRIBUTION DISPLAY METHOD, APPARATUS AND PROGRAM | |
| CN105716975A (en) | Material mechanical performance measurement device and pressing head assembly and measurement method thereof | |
| CN110793857A (en) | Device for measuring elongation of steel bar tensile test and using method thereof | |
| JP4811567B2 (en) | Stress measurement method for structures using photographed images | |
| CN214747560U (en) | Steel tape calibrating device | |
| JP7115201B2 (en) | Crack growth evaluation method | |
| KR20190118578A (en) | Insertion Force and In-Output Measurement System | |
| KR101677370B1 (en) | METHOD FOR AUTOMATIC VALUATION EQUIPMENT OF DWTT(Drop Weight Tear Test) WAVE SURFACE USING IMAGE | |
| CN202994595U (en) | Young modulus measurement experimental apparatus | |
| KR101264292B1 (en) | Resonant column testing apparatus with image-based analysis system for deformation modes of specimen using high speed camera | |
| JP2014102132A (en) | Low cycle fatigue crack growth evaluation method | |
| JP2004257925A (en) | Material testing machine | |
| CN110332902B (en) | A distributed optical fiber fixing device and method for deformation monitoring of anti-sliding piles | |
| CN114147144B (en) | A wire body straightening device and method | |
| US11175276B2 (en) | Fabric testing hardware | |
| CN107328331A (en) | The distributed steel straight ruler verification devices and methods therefor of view-based access control model |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 12832719 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 12832719 Country of ref document: EP Kind code of ref document: A1 |