US566629A - smillie - Google Patents
smillie Download PDFInfo
- Publication number
- US566629A US566629A US566629DA US566629A US 566629 A US566629 A US 566629A US 566629D A US566629D A US 566629DA US 566629 A US566629 A US 566629A
- Authority
- US
- United States
- Prior art keywords
- tube
- wire
- brackets
- wound
- furnace
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000002184 metal Substances 0.000 description 16
- 229910052751 metal Inorganic materials 0.000 description 16
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 4
- 229910000831 Steel Inorganic materials 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 3
- 239000000956 alloy Substances 0.000 description 3
- 229910045601 alloy Inorganic materials 0.000 description 3
- 229910052802 copper Inorganic materials 0.000 description 3
- 239000010949 copper Substances 0.000 description 3
- 238000007598 dipping method Methods 0.000 description 3
- 238000005260 corrosion Methods 0.000 description 2
- 230000007797 corrosion Effects 0.000 description 2
- 239000007789 gas Substances 0.000 description 2
- 229910052742 iron Inorganic materials 0.000 description 2
- 230000001681 protective effect Effects 0.000 description 2
- 206010059837 Adhesion Diseases 0.000 description 1
- 239000007990 PIPES buffer Substances 0.000 description 1
- ATJFFYVFTNAWJD-UHFFFAOYSA-N Tin Chemical compound [Sn] ATJFFYVFTNAWJD-UHFFFAOYSA-N 0.000 description 1
- 238000007596 consolidation process Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000005611 electricity Effects 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 230000004907 flux Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000004804 winding Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K9/00—Arc welding or cutting
- B23K9/0026—Arc welding or cutting specially adapted for particular articles or work
- B23K9/0035—Arc welding or cutting specially adapted for particular articles or work of thin articles
Definitions
- FIG-l- ⁇ No Model. 2 sneetksheeflz.
- My invention relates to the manufactureof pipes or tubes, and has for its object to pro vide an apparatus for the construction of pipes or tubes capable of withstanding high steam or other fluid or gaseous pressure.
- My invention consists ina new and improved apparatus by means of which a metal pipe or shell is provided with a covering or casing consisting of a spirally-wound strip or wire of steel or other metal.
- the consolidation of the strip or wire with the internal shell is effected by dipping into a bath of molten tin or other metal or alloy of sufficiently high fusing-point to be unaffected by the temperature of steam or other gas or gases for which the tube is designed, a suitable flux being employed to insure adhe sion between the molten metal or alloy and the wire or strip and the shell. This also protects the spirally-wound strips or wires from corrosion.
- iron or steel wire it is preferable to have the same cased with copper or other protective metal, so that the steel or iron or other metal core may not be deteriorated in the process of dipping in the molten bath.
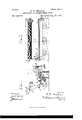
- Figure 1 represents a vertical central secti on through my apparatus.
- Fig. 2 represents a front elevation of the same.
- Fig. 3 represents an enlarged detail view of the mechanism for rotating the tube while being wound, parts being broken away; and
- Figs. 4, 5, and 6 represent enlarged longitudinal sections of pipes or tubes provided with different forms of spirally-wound strips or wires.
- My apparatus consists of a trough or bath for holding the molten metal into which the pipe is to be submerged while being wound,
- this trough is mounted upon a suitable framework of masonry, which constitutes the furnace for treating the bath.
- the tube while being wound is held by mandrels in suitable brackets and may be raised from or lowered into the bath by means of sui table means hereinafter to be described.
- the tube is rotated by means of suitable gearing, and the wire used for covering the tube is wound off from a coil suspended above the apparatus.
- D represents the trough for containing the bath of molten metal.
- This trough is preferably made semielliptical in cross-section and of sufficient length to receive a whole length of pipe, and is mounted upon a framework: of masonry, beneath which are the furnace Q and the return-flue T.
- the tube is held by mandrels K and K, carried by brackets B and B. These brackets are keyed upon a shaft E, pivotally supported in stands E rigidly mounted upon the framework of the masonry at one side of the trough D.
- the inner rod 1) of the bracket B carries a pair of gear-wheels II and H, the gear-wheel 11 being keyed upon the same shaft with the mandrel K.
- a sprocket-wheel F is keyed upon the same shaft with the gear-wheel H.
- the sprocket wheel F is driven by a sprocketchain which engages the sprocket-wheel F.
- the sprocket-wheel F is driven by the pulley E, both saidsprocket-wheel and. said pulley being loosely mounted upon the shaft E, as shown most clearly in Fig.
- the pulley E is driven by a belt from any suitable source of power, and through the intermediate gearing just described causes the mandrel II to rotate with the tube.
- I may use some other suitable gearing, and I show and 2 V r V r 566,629
- the bracketB has an outwardly-extending.
- P represents the drum from which the wire YV is wound upon the tube. This drum is suspended from suitable hangers'S, and a friction-lever N, carrying a Weight n, is provided upon the shaft of this drum for giving tension to the wire being unwound.
- Rollers R, R, and R over which the: wire runs are revolubly mounted in stands upon the masonry, and a pulley IV, carrying a weight w, is suspended from a loop in the wire between the rollers R and R to give additional tension to the wire and to take up the slack should the tube be lifted from the bath during the operation of winding.
- the pipe A (shown in Fig. 4) is represented as wound with a metallic strip, rectangular in cross-section.
- the pipe A (shown in Fig. 4) is represented as wound with a metallic strip, rectangular in cross-section.
- the pipe A (shown in Fig. 4) is represented as wound with a metallic strip, rectangular in cross-section.
- the pipe A (shown in Fig. 4) is represented as wound with a metallic strip, rectangular in cross-section.
- -' 'a trough for containing molten metal mounted above said furnace; means for holding the tube in said molten bath While being wound; means for rotating said tube in said bath; a drum provided with a friction device from which the Wire is fed to said tube while being wound; tension devices for holding said wire taut; and means for raising and lowering said tube into said bath, substantially as and for the purposes described.
- a furnace, and a trough for containing molten metal mounted above said furnace; a pair of pivoted brackets carrying mandrels for holding the tube; an arm on one of said brackets terminating in a toothed quadrant; a worm adapted to engage said toothed quadrant, for imparting a rocking motion to said brackets, and thus raising or lowering the tube carried by said mandrels; a pair of toothed gear-wheels carried by one of said brackets and adapted to rotate one of said mandrels; a pulley mounted upon a shaft in line with the axis of said brackets and adapted to be driven from any suitable source of power; driving-gear between said pulley and said gear-wheels; a drum from which the wire is fed to said tube while being wound; and tension devices for holding said wire taut, substantially as described.
Landscapes
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Mechanical Engineering (AREA)
- Vertical, Hearth, Or Arc Furnaces (AREA)
Description
(No Model.) 2 ShQetB- -Sheet 1. R. D. SMILLIE.
APPARATUS FOR MAKING STEAM PIPES. No. 566,629. Patented Aug. 25, 1896;
FIE-.2-
FIG-l- {No Model.) 2 sneetksheeflz.
R. D. SMILLIE.
APPARATUS FOR MAKING STEAM PIPES.
N0. 566,62Q. Patented Aug. 25, 1896.
mg cams nevus co. mcr au'mo" WASHWGYO". JV :2
UNITED STATES ROBERT DANIEL SMILL'IE,
PATENT @rricn.
OF GLASGOW, SCOTLAND.
APPARATUS FOR MAKING STEAM-PIPES.
SPECIFICATION forming part of Letters Patent No. 566,629, dated August 25, 1896.
A ii fi fil d June 13, 1895. Serial No. 552,722. (No modeli) Patented in England September 12, 1893, No. 17,101.
To aZZ whom it may concern:
Be it known that 1, ROBERT DANIEL SMIL- LIE, electrical engineer, residing at 80 Mains Street, Glasgow, Scotland, have invented certain new and useful Improvements in Apparatus for the Manufacture of Pipes or Tubes, (for which I have,with another, obtained Let ters Patent of Great Britain, No. 17,101 dated September 12, 1893 and I do hereby declare the following to be a full, clear, and exact description of the invention, such as will enable others skilled in the art to which it appertains to make and use the same.
My invention relates to the manufactureof pipes or tubes, and has for its object to pro vide an apparatus for the construction of pipes or tubes capable of withstanding high steam or other fluid or gaseous pressure.
My invention consists ina new and improved apparatus by means of which a metal pipe or shell is provided with a covering or casing consisting of a spirally-wound strip or wire of steel or other metal.-
The consolidation of the strip or wire with the internal shell is effected by dipping into a bath of molten tin or other metal or alloy of sufficiently high fusing-point to be unaffected by the temperature of steam or other gas or gases for which the tube is designed, a suitable flux being employed to insure adhe sion between the molten metal or alloy and the wire or strip and the shell. This also protects the spirally-wound strips or wires from corrosion.
In the case of iron or steel wire being used it is preferable to have the same cased with copper or other protective metal, so that the steel or iron or other metal core may not be deteriorated in the process of dipping in the molten bath.
My invention will be understood by reference to the accompanying drawings, wherein the same parts are indicated by the same letters throughout the several views.
Figure 1 represents a vertical central secti on through my apparatus. Fig. 2 represents a front elevation of the same. Fig. 3 represents an enlarged detail view of the mechanism for rotating the tube while being wound, parts being broken away; and Figs. 4, 5, and 6 represent enlarged longitudinal sections of pipes or tubes provided with different forms of spirally-wound strips or wires. My apparatus consists of a trough or bath for holding the molten metal into which the pipe is to be submerged while being wound,
and this trough is mounted upon a suitable framework of masonry, which constitutes the furnace for treating the bath.
The tube while being wound is held by mandrels in suitable brackets and may be raised from or lowered into the bath by means of sui table means hereinafter to be described.
The tube is rotated by means of suitable gearing, and the wire used for covering the tube is wound off from a coil suspended above the apparatus.
To describe my apparatus -more fully, D represents the trough for containing the bath of molten metal. This trough is preferably made semielliptical in cross-section and of sufficient length to receive a whole length of pipe, and is mounted upon a framework: of masonry, beneath which are the furnace Q and the return-flue T.
The tube is held by mandrels K and K, carried by brackets B and B. These brackets are keyed upon a shaft E, pivotally supported in stands E rigidly mounted upon the framework of the masonry at one side of the trough D.
The inner rod 1) of the bracket B carries a pair of gear-wheels II and H, the gear-wheel 11 being keyed upon the same shaft with the mandrel K. A sprocket-wheel F is keyed upon the same shaft with the gear-wheel H. The sprocket wheel F is driven by a sprocketchain which engages the sprocket-wheel F. The sprocket-wheel F is driven by the pulley E, both saidsprocket-wheel and. said pulley being loosely mounted upon the shaft E, as shown most clearly in Fig.
The pulley E is driven by a belt from any suitable source of power, and through the intermediate gearing just described causes the mandrel II to rotate with the tube. Instead of this form of driving mechanism, I may use some other suitable gearing, and I show and 2 V r V r 566,629
The bracketB has an outwardly-extending.
arm 13 which terminates in atoothed quadrant 2), which engages a Worm M. V This worm M is rotated by means of the hand wheel m, and the bracketB is thereby given a rocking motion to lower the tube into the bath or raise it from the same and hold it in the desired position.
P represents the drum from which the wire YV is wound upon the tube. This drum is suspended from suitable hangers'S, and a friction-lever N, carrying a Weight n, is provided upon the shaft of this drum for giving tension to the wire being unwound.
Rollers R, R, and R over which the: wire runs, are revolubly mounted in stands upon the masonry, and a pulley IV, carrying a weight w, is suspended from a loop in the wire between the rollers R and R to give additional tension to the wire and to take up the slack should the tube be lifted from the bath during the operation of winding.
The pipe A (shown in Fig. 4) is represented as wound with a metallic strip, rectangular in cross-section. The pipe A (shown in Fig.
5) is represented as wound with small steel wire incased in copper or other protective metal, and the pipe A Fig. 5, is represented as wound with larger wire and not inclosed in a casing of copper.
In some cases it may be advisable, after dipping in the molten bath, to deposit by electricity a metal or alloy to protect the consolidated tube from corrosion.
Having thus described my invention, what I claim, and desire to secure by Letters Patent of the United States, is
1. Inlan apparatus of the character describbd, the combination with a furnace, and
-' 'a trough for containing molten metal mounted above said furnace; means for holding the tube in said molten bath While being wound; means for rotating said tube in said bath; a drum provided with a friction device from which the Wire is fed to said tube while being wound; tension devices for holding said wire taut; and means for raising and lowering said tube into said bath, substantially as and for the purposes described.
2. In an apparatus of the character described, the combination with a furnace, and a trough for containing molten metal mounted above said furnace; a pair of pivoted brackets each carrying at one end amandrel for holding the tube,'an arm on one of said brackets terminating in atoothed quadrant; a worm adapted to engage said toothed quadrant for imparting a rocking motion to said brackets and thus raising or lowering the tube carried by said mandrels; means for rotating said tube; a 'drum'provided with a friction device from which the wire is fed to 7 said tube while being wound and tension devices for holding said wire taut, substantially as and forthe purposes described.
3. In an apparatus of. the character described, the combination with a furnace, and a trough for containing molten metal mounted above said furnace; a pair of brackets pivoted upon suitable stands mounted above said furnace; a mandrel carried by one end of each ofsaid brackets; means for rotating one of said mandrels; an arm on one of said brackets terminating in a toothed quadrant; a worm adapted to engage said toothed quadrant; means for turning said worm and imparting a rocking motion to said brackets; and a drum from which the wire is fed to the tube being wound, substantially as described.
4:. In an apparatus of the character described, the combination. with a furnace, and r a trough for containing molten metal mountied above said furnace; a pairof brackets pivoted upon suitable stands mounted above said furnace, a mandrel carried by one end of each of said brackets; an arm on oneof said brackets terminating in a toothed quadrant; a Worm adapted to engage said toothed quadrant, a hand-wheel for turning said Worm and imparting a rocking motion to said brackets; a pulley having its axis in line with the axis of said pivoted brackets, and adapted to be driven from any suitable source of power; drivingear between said pulley and one of said mandrels, for rotating the same; and a drum from which the wire is fed to the tube being wound, substantially as described.
5. In an apparatus of the character described, the combination of a furnace, and a trough for containing molten metal mounted above said furnace; a pair of pivoted brackets carrying mandrels for holding the tube; an arm on one of said brackets terminating in a toothed quadrant; a worm adapted to engage said toothed quadrant, for imparting a rocking motion to said brackets, and thus raising or lowering the tube carried by said mandrels; a pair of toothed gear-wheels carried by one of said brackets and adapted to rotate one of said mandrels; a pulley mounted upon a shaft in line with the axis of said brackets and adapted to be driven from any suitable source of power; driving-gear between said pulley and said gear-wheels; a drum from which the wire is fed to said tube while being wound; and tension devices for holding said wire taut, substantially as described.
IIS
6. In an apparatus of the character described, the combination of a furnace, and a trough for containing molten metal mounted above said furnace; means for holding the tube in said molten bath while being wound; means for rotating said tube; means for raising said tube from and lowering said tube into said bath; and devices for feeding the wire to said tube under tension while being wound, substantially as described. I0
In testimony whereof I affix my signature in presence of two witnesses.
ROBERT DANIEL SMILLIE. Witnesses:
JNO. B. LEES, JAS. A. THOMSON.
Publications (1)
| Publication Number | Publication Date |
|---|---|
| US566629A true US566629A (en) | 1896-08-25 |
Family
ID=2635339
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US566629D Expired - Lifetime US566629A (en) | smillie |
Country Status (1)
| Country | Link |
|---|---|
| US (1) | US566629A (en) |
-
0
- US US566629D patent/US566629A/en not_active Expired - Lifetime
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105382034B (en) | High speed cold rolled reinforcing bar uncoiling automatic lead feeding device | |
| US334709A (en) | Oooooo oooo | |
| US2870903A (en) | Metal drawing lubricant | |
| JP4909098B2 (en) | Metal foil threading equipment | |
| US423445A (en) | Apparatus for heating continuous lengths of rods | |
| US375435A (en) | Machine for making spi rally-jointed metal tubes | |
| US1476632A (en) | Method of manufacturing tubes | |
| CN210945684U (en) | A telescopic lifting mechanism for steel wire water bath heating treatment | |
| US3495785A (en) | Method and apparatus for winding metal strip for open-coil annealing and resulting coil | |
| US575389A (en) | Side iron works | |
| US285124A (en) | Welding apparatus | |
| US1616861A (en) | Method and apparatus for manufacturing tubing | |
| US1293486A (en) | Welding device. | |
| US508370A (en) | William a | |
| US636157A (en) | Apparatus for manufacturing chains. | |
| US1351348A (en) | A cobpobation of new jebsey | |
| US557479A (en) | Draw bench for manufacturing pipe | |
| US606159A (en) | apparatus for manufacturing pipe | |
| US510352A (en) | Esther logan adminis | |
| US1505994A (en) | Tinning machine | |
| US1671731A (en) | Method and apparatus for the manufacture of tubes | |
| US1861421A (en) | Method of making tubing | |
| US978543A (en) | Machine for soldering chains. | |
| US720046A (en) | Apparatus for the manufacture of butt-weld pipe. | |
| US573632A (en) | Wire-fence machine |