KR20200056661A - Furniture Top Plate using Synthetic Resin and Wood and Manufacturing Method Thereof - Google Patents
Furniture Top Plate using Synthetic Resin and Wood and Manufacturing Method Thereof Download PDFInfo
- Publication number
- KR20200056661A KR20200056661A KR1020180140604A KR20180140604A KR20200056661A KR 20200056661 A KR20200056661 A KR 20200056661A KR 1020180140604 A KR1020180140604 A KR 1020180140604A KR 20180140604 A KR20180140604 A KR 20180140604A KR 20200056661 A KR20200056661 A KR 20200056661A
- Authority
- KR
- South Korea
- Prior art keywords
- synthetic resin
- wood
- furniture
- top plate
- primer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- A—HUMAN NECESSITIES
- A47—FURNITURE; DOMESTIC ARTICLES OR APPLIANCES; COFFEE MILLS; SPICE MILLS; SUCTION CLEANERS IN GENERAL
- A47B—TABLES; DESKS; OFFICE FURNITURE; CABINETS; DRAWERS; GENERAL DETAILS OF FURNITURE
- A47B96/00—Details of cabinets, racks or shelf units not covered by a single one of groups A47B43/00 - A47B95/00; General details of furniture
- A47B96/20—Furniture panels or like furniture elements
- A47B96/205—Composite panels, comprising several elements joined together
-
- A—HUMAN NECESSITIES
- A47—FURNITURE; DOMESTIC ARTICLES OR APPLIANCES; COFFEE MILLS; SPICE MILLS; SUCTION CLEANERS IN GENERAL
- A47B—TABLES; DESKS; OFFICE FURNITURE; CABINETS; DRAWERS; GENERAL DETAILS OF FURNITURE
- A47B13/00—Details of tables or desks
- A47B13/08—Table tops; Rims therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D3/00—Pretreatment of surfaces to which liquids or other fluent materials are to be applied; After-treatment of applied coatings, e.g. intermediate treating of an applied coating preparatory to subsequent applications of liquids or other fluent materials
- B05D3/12—Pretreatment of surfaces to which liquids or other fluent materials are to be applied; After-treatment of applied coatings, e.g. intermediate treating of an applied coating preparatory to subsequent applications of liquids or other fluent materials by mechanical means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D7/00—Processes, other than flocking, specially adapted for applying liquids or other fluent materials to particular surfaces or for applying particular liquids or other fluent materials
- B05D7/06—Processes, other than flocking, specially adapted for applying liquids or other fluent materials to particular surfaces or for applying particular liquids or other fluent materials to wood
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D7/00—Processes, other than flocking, specially adapted for applying liquids or other fluent materials to particular surfaces or for applying particular liquids or other fluent materials
- B05D7/24—Processes, other than flocking, specially adapted for applying liquids or other fluent materials to particular surfaces or for applying particular liquids or other fluent materials for applying particular liquids or other fluent materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D7/00—Processes, other than flocking, specially adapted for applying liquids or other fluent materials to particular surfaces or for applying particular liquids or other fluent materials
- B05D7/50—Multilayers
- B05D7/52—Two layers
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J7/00—Chemical treatment or coating of shaped articles made of macromolecular substances
- C08J7/04—Coating
-
- A—HUMAN NECESSITIES
- A47—FURNITURE; DOMESTIC ARTICLES OR APPLIANCES; COFFEE MILLS; SPICE MILLS; SUCTION CLEANERS IN GENERAL
- A47B—TABLES; DESKS; OFFICE FURNITURE; CABINETS; DRAWERS; GENERAL DETAILS OF FURNITURE
- A47B2220/00—General furniture construction, e.g. fittings
- A47B2220/008—General furniture construction, e.g. fittings characterised by materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D2203/00—Other substrates
- B05D2203/20—Wood or similar material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D2451/00—Type of carrier, type of coating (Multilayers)
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D2504/00—Epoxy polymers
Landscapes
- Engineering & Computer Science (AREA)
- Life Sciences & Earth Sciences (AREA)
- Wood Science & Technology (AREA)
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Mechanical Engineering (AREA)
- Tables And Desks Characterized By Structural Shape (AREA)
Abstract
합성수지와 목재를 이용한 가구용 상판 및 그 제조방법에 관한 것으로, (a) 목재부재를 선별하는 단계; (b) 선별된 목재부재 중 한 쌍의 상기 목재부재를 상판틀의 양 측면에 밀착시켜 이격된 한 쌍의 목재부재 사이에 합성수지부재가 성형되도록 안착시키는 단계; (c) 상기 한 쌍의 목재부재 사이에 소정 두께로 합성수지를 부어 경화시키는 과정을 반복적으로 하여 상기 한 쌍의 목재부재 사이에 상기 목재부재와 동일한 높이로 합성수지부재를 성형하는 단계; (d) 상기 한 쌍의 목재부재 및 상기 프라이머에 의해 형성된 합성수지부재의 상면을 고르게 평판화시키는 단계; (e) 상기 한 쌍의 목재부재 및 상기 합성수지부재로 이루어진 가구용 상판의 표면을 샌딩하는 단계; (f) 상기 가구용 상판의 표면에 소정의 두께로 코팅하는 단계; (g) 상기 가구용 상판의 코팅면에 왁스를 코팅하는 단계;를 마련하여 한 쌍의 목재부재 사이에 합성수지부재를 성형함으로써 목재와 투명한 합성수지에 의한 심미감을 가질 수 있고, 투명 또는 다양한 색상을 갖는 합성수지부재를 목재부재 사이에 일체로 성형할 수 있으며, 합성수지부재 내에 자갈, 소라 등의 천연소재를 넣어 가구용 및 인테리어용으로 사용할 수 있다는 효과가 얻어진다.A method for manufacturing a top plate for furniture using synthetic resin and wood, and a method for manufacturing the same, comprising: (a) selecting a wooden member; (B) step of placing a pair of the wood member of the selected wood member in close contact with both sides of the upper frame to form a synthetic resin member between the spaced pair of wood members; (c) forming a synthetic resin member at the same height as the wooden member between the pair of wooden members by repeatedly performing a process of pouring and curing a synthetic resin with a predetermined thickness between the pair of wooden members; (d) evenly flattening the upper surfaces of the pair of wood members and the synthetic resin member formed by the primer; (E) sanding the surface of the top plate for furniture made of the pair of wood members and the synthetic resin member; (f) coating the surface of the furniture top plate with a predetermined thickness; (g) coating the wax on the coating surface of the furniture top plate; by forming a synthetic resin member between a pair of wooden members, it can have an aesthetic sense by wood and a transparent synthetic resin, and a synthetic resin having a transparent or various colors The member can be integrally molded between the wooden members, and the effect of being able to be used for furniture and interior is obtained by putting natural materials such as gravel and turban in the synthetic resin member.
Description
본 발명은 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법에 관한 것으로, 더욱 상세하게는 2개의 이격된 목재 사이에 합성수지로 목재와 동일한 높이의 상판을 형성하여 테이블, 문짝, 싱크볼, 테이블, 장롱 등의 가구 및 인테리어용으로 사용할 수 있는 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법에 관한 것이다.The present invention relates to a top plate for furniture using synthetic resin and wood and a method for manufacturing the same, and more specifically, to form a top plate of the same height as a synthetic resin between two spaced woods, such as a table, a door, a sink ball, a table, a wardrobe, etc. It relates to a top plate for furniture using synthetic resin and wood that can be used for furniture and interior, and a method for manufacturing the same.
일반적으로 가구의 하나인 책상, 탁자, 테이블은, 책을 읽거나 음식물을 섭취하거나 다양한 사무를 보기 위한 것으로, 상면이 평편한 면으로 이루어진 상판과, 상기 상판의 하부에 고정되어 지면에 대하여 지지하도록 된 다리를 포함하여 이루어진다.In general, a desk, table, and table, which is one of furniture, is for reading a book, eating food, or viewing various office work, and the upper surface is made of a flat surface and is fixed to the lower portion of the upper surface to support the ground. It is made including the legs.
이러한 가구용 상판은 나무 재질 또는 금속 및 합성수지 재질의 '판넬'로 이루어지며, 다수의 판이 서로 조립되면서 하나의 완성된 상판을 형성하도록 된 조립식 구조가 적용된 상판이 있다.The top plate for furniture is made of a 'panel' made of wood or metal and synthetic resin, and there is a top plate to which a prefabricated structure is applied to form one completed top plate as multiple plates are assembled with each other.
가구에 적용되는 소재는 목재, 금속, 대리석 등의 재료가 주로 사용되며, 경우에 따라 재료의 표면에 소정 두께를 갖는 유리 또는 시트지가 부착된 상태로 사용되고 있다.Materials used for furniture are mainly used materials such as wood, metal, and marble, and in some cases, glass or sheet paper having a predetermined thickness is attached to the surface of the material.
가구 재료로 금속 또는 대리석이 사용되는 경우, 내구성이 좋은 반면 무게가 무거워 설치 및 운반에 어려움이 있었고, 가구 재료로 목재가 사용되는 경우, 대부분 원목이 그대로 사용됨에 따라 비용이 상승되는 문제점이 있었다.When a metal or marble is used as a furniture material, it is difficult to install and transport due to its high weight while being durable, and when wood is used as a furniture material, there is a problem in that cost increases as most of the wood is used as it is.
목재는 수분의 흡수와 증발에 따른 수축과 팽창을 하는 특성을 가지고 있어서 가구 제작용으로 이용되기 위해서는 가구 제작에 적합한 함수율(10~12%)에 이르도록 건조된다. 또한 가구 제작용으로 이용되는 목재는 치수안정을 위해 약품처리 등 여러가지 공정을 거치게 된다.Wood has the property of shrinking and expanding due to absorption of water and evaporation, so it is dried to reach a moisture content (10 to 12%) suitable for furniture production to be used for furniture production. In addition, wood used for furniture is subjected to various processes such as chemical treatment for dimensional stability.
가구는 목재의 종류에 따라 원목 가구, 인공판재 가구, 천연무늬목 가구 등으로 구분된다. 원목 가구는 최고 품질을 갖지만 가격이 고가이다. 원목은 시간 지날수록 그 특징과 매력이 오히려 증가하여 오래 사용할 수 있다.Furniture is classified into wood furniture, artificial wood furniture, natural veneer furniture, etc., depending on the type of wood. Solid wood furniture has the highest quality but is expensive. Solid wood can be used for a long time because its characteristics and attractiveness increase over time.
특히 경목재 원목은 낙엽수나 활엽수 통나무의 줄기를 잘라 만들며, 오크(참나무)와 단풍나무가 대표적인 가구용 원목이다.In particular, hardwood logs are made by cutting the trunks of deciduous trees and broad-leaved logs, and oak (oak) and maple trees are typical wood for furniture.
인공판재 가구는 합성목재를 이용하는 것으로, 가구용 합성목재로는 MDF(Medium Density Fiberboard)와 PB(Partcle Board)가 대표적이다.Artificial wood furniture is made of synthetic wood, and MDF (Medium Density Fiberboard) and PB (Partcle Board) are typical synthetic wood for furniture.
MDF는 강력한 열과 압력하에서 접착제로 목재섬유를 접착하여 만든 것으로, 가격이 저렴하고 어느 정도의 내구성을 갖는다.MDF is made by bonding wood fibers with an adhesive under strong heat and pressure. It is inexpensive and has some durability.
MDF는 저렴한 비용으로 진짜 나무처럼 보이게 하는 장점이 있고, 못질이 가능할 정도로 단단하며 가볍다. PB는 목재, 대나무, 아마, 사탕수수 등의 리그노셀룰로이드 성분을 재료로 기계적으로 분쇄하여 파티클로 만든 다음 건조시키고 접착제를 혼합하여 성형시킨 후 열압하여 만든 것이다.MDF has the advantage of making it look like real wood at a low cost, and is hard and light enough to be nailed. PB is made by mechanically pulverizing lignocelluloid components such as wood, bamboo, flax, and sugar cane into particles, then drying, mixing and molding the adhesive, and then heat-pressing.
PB는 목재, 합판, MDF에 비해 가격이 저렴하나, 충력에 약하고 무거운 단점이 있다.PB is cheaper than wood, plywood, and MDF, but it has weak drawbacks and weak weight.
천연무늬목 가구는 천연 나무에서 썰어진 얇은 조각으로 만들어진 천연무늬목으로 만들어지고, 실제 나무인 것처럼 보여지기 위해 원목, MDF, PB 등의 가구 재료 위에 접착된다.Natural veneer furniture is made of natural veneer made of thin pieces sliced from natural wood, and is glued on furniture materials such as wood, MDF, PB, etc. in order to appear to be real wood.
무늬목은 가구재료 위에 저렴하게 입힐 수 있고 가벼운 특성이 있다. 천연무늬목은 원목, MDF, PB 처럼 부드럽고 평평한 재료이면 무엇이든 적용이 가능하여 다양하면서 보편적인 가구 제조 방법으로 이용된다.The veneer can be coated on furniture materials inexpensively and has light properties. Natural veneer can be applied to any soft, flat material such as solid wood, MDF, PB, and is used as a variety of universal furniture manufacturing methods.
예를 들어, 하기 특허문헌 1에는 '가구용 조립식 상판'이 개시되어 있다.For example, Patent Document 1 below discloses a 'prefabricated top plate for furniture'.
하기 특허문헌 1에 따른 가구용 조립식 상판은 상면이 평편한 면으로 이루어진 '판(板:plate)' 형상의 판체로 형성되며 하부에는 지면에 대하여 지지하도록 된 다리가 결합하도록 된 고정수단과, 상기 고정수단에 각각 고정되는 다수의 조립블록들의 결합을 통해 형성되어 '판(板"plate)' 형상을 형성하도록 된 몸체와, 상기 조립블록들의 저면에 형성된 결합홈과, 상기 고정수단의 상면에 상부로 돌출 형성된 결합돌기로 이루어져 상기 조립블록의 저면과 상기 고정수단의 상면을 서로 끼워 맞춤 결합하도록 된 결합수단을 포함한다.The prefabricated top plate for furniture according to Patent Document 1 below is formed of a plate body having a 'plate' shape having a flat top surface, and at the bottom, fixing means configured to engage legs supported to support the ground, and the fixing The body is formed through a combination of a plurality of assembly blocks that are fixed to each means to form a 'plate' shape, a coupling groove formed on the bottom surface of the assembly blocks, and an upper surface of the fixing means. It comprises a coupling means formed by protruding coupling protrusions to fit and fit the bottom surface of the assembly block and the upper surface of the fixing means.
상기 조립블록의 상기 결합홈의 중앙에 상기 결합돌기의 길이방향으로 돌출형성된 체결봉과, 상기 고정수단의 결합돌기의 중앙에 형성되며 상기 체결봉이 관통하면서 결합하는 체결공과, 상기 고정수단의 저면에서 상기 체결봉의 종단을 고정하여 상기 체결봉이 무단으로 상기 체결공에서 분리되지 않도록 고정하는 체결캡을 포함하여 이루어지는 체결수단을 더 포함한다.A fastening rod protruding in the longitudinal direction of the engaging projection in the center of the engaging groove of the assembly block, a fastening hole formed in the center of the engaging projection of the fixing means and coupled while the fastening rod penetrates, the bottom of the fixing means It further comprises a fastening means comprising a fastening cap to fix the end of the fastening rod so that the fastening rod is not separated from the fastening hole without permission.
상기 체결봉의 종단에는 상기 체결봉의 길이방향으로 형성된 절개홈이 구비되며, 외측테두리에는 외측방향으로 연장 형성된 걸림돌부가 구비되고, 상기 체결캡에는 상기 체결봉의 종단이 관통하면서 수용되는 관통공이 형성되며, 상단 내측면에 상기 걸림돌부가 탄성적으로 탄지되어 지지고정되는 걸림턱이 형성된다.The end of the fastening rod is provided with an incision groove formed in the longitudinal direction of the fastening rod, an outer frame is provided with a locking protrusion extending in the outer direction, and the fastening cap is formed with a through hole that is accommodated while the end of the fastening rod penetrates, the top On the inner side, a locking jaw is formed by elastically supporting the locking protrusion by being supported.
하기 특허문헌 2에는 '가구의 상판'이 개시되어 있다.Patent Document 2 below discloses a 'top of furniture'.
하기 특허문헌 2에 따른 가구의 상판은 상면을 갖는 제1 측면 지지목 및 제2 측면 지지목, 일단이 상기 제1 측면 지지목에 고정되고 타단이 상기 제2 측면 지지목에 고정되어 상기 제1 측면 지지목과 상기 제2 측면 지지목을 상호 평행하게 결합하는 복수의 버팀목, 상면을 갖고 상기 제1 측면 지지목과 상기 제2 측면 지지목 사이와 상기 복수의 버팀목 위에 배치되는 복수의 상면목 및 상기 제1 측면 지지목과 상기 제2 측면 지지목에 배치되는 상기 복수의 상면목 중 최외곽에 배치되는 두 상면목과 각각 접하도록 상기 제1 측면 지지목과 상기 제2 측면 지지목 사이에 배치되는 제1 말단목 및 제 2 말단목을 포함한다.The upper side of the furniture according to the following patent document 2 has a first side support tree and a second side support tree having an upper surface, one end is fixed to the first side support tree and the other end is fixed to the second side support tree, and the first A plurality of struts for coupling a side support tree and the second side support tree in parallel with each other, a plurality of upper surface trees having a top surface and disposed between the first side support tree and the second side support tree and over the plurality of support trees and the agent A first end tree disposed between the first side support tree and the second side support tree so as to be in contact with the two top surface trees respectively disposed on the outermost side of the one side support tree and the plurality of top surface trees disposed on the second side support tree. And a second extremity.
상기 상면목들과 상기 측면 지지목들 중 어느 한쪽에는 상기 측면 지지목들의 길이 방향으로 연장된 삽입홈이 마련되고, 다른 한쪽에는 상기 삽입홈에 삽입되는 삽입돌기가 구비되어 상기 상면목들은 상기 측면 지지목들의 길이 방향으로 슬라이드 이동할 수 있고, 상기 측면 지지목들과 상기 말단목들 중 어느 한쪽에는 상기 측면 지지목들의 길이 방향으로 연장된 레일 돌기가 마련된다.One of the upper surface necks and the side support trees is provided with an insertion groove extending in the longitudinal direction of the side support trees, and the other side is provided with an insertion protrusion inserted into the insertion groove so that the upper surface trees have the side It is possible to slide in the longitudinal direction of the support necks, and either one of the side support necks and the end necks is provided with rail projections extending in the length direction of the side support necks.
다른 한쪽에는 상기 레일 돌기가 삽입되는 레일 홈이 마련되어 상기 말단목들은 상기 측면 지지목들의 길이 방향으로 슬라이드 이동할 수 있으며, 상기 버팀목과 상기 측면 지지목들 중 어느 한 쪽에는 상기 버팀목을 상기 측면 지지목들에 고정하기 위한 고정홈이 마련되고, 다른 한쪽에는 상기 고정홈에 삽입되는 고정 돌기가 형성된다.On the other side, a rail groove into which the rail protrusion is inserted is provided so that the end necks can slide in the longitudinal direction of the side support necks, and either one of the support necks and the side support necks supports the support necks to the side support woods. A fixing groove for fixing to the field is provided, and a fixing protrusion inserted into the fixing groove is formed on the other side.
본 발명의 목적은 상기한 바와 같은 문제점을 해결하기 위한 것으로, 2개의 목재 사이에 다양한 형상과 모양을 갖는 합성수지를 일체화시켜 가구용 또는 인테리어용으로 사용할 수 있도록 하는 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법을 제공하는 것이다.The object of the present invention is to solve the problems as described above, by combining the synthetic resin having a variety of shapes and shapes between two wood to be used for furniture or interiors and synthetic resins and furniture tops using wood and its manufacturing Is to provide a way.
본 발명의 다른 목적은 원목의 질감과 함께 합성수지에 의한 다양한 색상 및 투명, 가구용 상판 내부에 돌, 자갈 등의 자연 소재를 함침시켜 자연적인 느낌을 연상시킬 수 있도록 하는 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법을 제공하는 것이다.Another object of the present invention is a variety of colors and transparency by the synthetic resin along with the texture of the raw wood, the interior of the furniture top plate for impregnating natural materials such as stone, gravel, etc. to make the natural feel reminiscent of furniture and the top plate for furniture using wood and It is to provide the manufacturing method.
상기한 바와 같은 목적을 달성하기 위하여, 본 발명에 따른 합성수지와 목재를 이용한 가구용 상판은 소정의 높이 및 소정의 길이를 갖도록 목재를 소정의 길이로 절단하여 형성된 제1 목재부재와 제2 목재부재; 소정의 간격만큼 이격된 상기 제1 목재부재와 상기 제2 목재부재 사이에 형성되는 합성수지부재;를 포함하는 것을 특징으로 한다.In order to achieve the above object, the top plate for furniture using synthetic resin and wood according to the present invention includes a first wood member and a second wood member formed by cutting wood to a predetermined length to have a predetermined height and a predetermined length; And a synthetic resin member formed between the first wood member and the second wood member spaced apart by a predetermined interval.
상기 합성수지부재는 자갈, 소라 등의 천연소재가 함침되며, 상기 합성수지부재는 내부에 함침된 천연소재가 외부로 노출되도록 투명하게 형성되고, 상기 합성수지부재의 색상이 다양한 색상 중 어느 하나로 이루어지는 것을 특징으로 한다.The synthetic resin member is impregnated with natural materials such as gravel and turban, and the synthetic resin member is transparently formed so that the impregnated natural material is exposed to the outside, and the color of the synthetic resin member is made of any one of various colors. do.
또한 본 발명에 따른 합성수지와 목재를 이용한 가구용 상판의 제조방법은 (a) 목재부재를 선별하는 단계; (b) 선별된 목재부재 중 한 쌍의 상기 목재부재를 상판틀의 양 측면에 밀착시켜 이격된 한 쌍의 목재부재 사이에 합성수지부재가 성형되도록 안착시키는 단계; (c) 상기 한 쌍의 목재부재 사이에 소정 두께로 합성수지를 부어 경화시키는 과정을 반복적으로 하여 상기 한 쌍의 목재부재 사이에 상기 목재부재와 동일한 높이로 합성수지부재를 성형하는 단계; (d) 상기 한 쌍의 목재부재 및 상기 프라이머에 의해 형성된 합성수지부재의 상면을 고르게 평판화시키는 단계; (e) 상기 한 쌍의 목재부재 및 상기 합성수지부재로 이루어진 가구용 상판의 표면을 샌딩하는 단계; (f) 상기 가구용 상판의 표면에 소정의 두께로 코팅하는 단계; (g) 상기 가구용 상판의 코팅면에 왁스를 코팅하는 단계;를 포함하는 것을 특징으로 한다.In addition, a method for manufacturing a top plate for furniture using synthetic resin and wood according to the present invention includes: (a) selecting a wooden member; (B) step of placing a pair of the wood member of the selected wood member in close contact with both sides of the upper frame to form a synthetic resin member between the spaced pair of wood members; (c) forming a synthetic resin member at the same height as the wooden member between the pair of wooden members by repeatedly performing a process of pouring and curing a synthetic resin with a predetermined thickness between the pair of wooden members; (d) evenly flattening the upper surfaces of the pair of wood members and the synthetic resin member formed by the primer; (E) sanding the surface of the top plate for furniture made of the pair of wood members and the synthetic resin member; (f) coating the surface of the furniture top plate with a predetermined thickness; (g) coating the wax on the coating surface of the furniture top plate; characterized in that it comprises a.
상기 (c) 단게에서, (c1) 상기 한 쌍의 목재부재 사이에 소정 두께로 합성수지를 부어 경화시키는 하도 프라이머 성형 단계; (c2) 상기 하도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 중도 프라이머 성형 단계; (c3) 상기 중도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 상도 프라이머 성형 단계;를 포함하는 것을 특징으로 한다.In the step (c), (c1) primer primer forming step of curing by pouring a synthetic resin to a predetermined thickness between the pair of wood members; (c2) a middle primer forming step of pouring a synthetic resin on the primer to cure to a predetermined thickness; (c3) a top coat primer forming step of pouring a synthetic resin on the middle primer to cure to a predetermined thickness.
상기 (c) 단계에서, 상기 프라이머 성형 단계는 프라이머를 소정 두께로 부어 경화시킨 다음 재차 프라이머를 부어 소정 두께로 경화시키는 과정이 반복적으로 이루어지는 것을 특징으로 한다.In the step (c), the primer forming step is characterized in that the primer is poured to a predetermined thickness to cure, and then the primer is poured again to cure to a predetermined thickness.
상기 (f) 단계에서, 상기 합성수지부재의 황변현상 및 스크래치가 발생되지 않도록 하이브리드 에폭시를 스프레이 작업에 의해 나노 코팅이 이루어지는 것을 특징으로 한다.In the step (f), nano-coating is performed by spraying a hybrid epoxy to prevent yellowing and scratching of the synthetic resin member.
상술한 바와 같이, 본 발명에 따른 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법에 의하면, 한 쌍의 목재부재 사이에 합성수지부재를 성형함으로써 목재와 투명한 합성수지에 의한 심미감을 가질 수 있고, 투명 또는 다양한 색상을 갖는 합성수지부재를 목재부재 사이에 일체로 성형할 수 있으며, 합성수지부재 내에 자갈, 소라 등의 천연소재를 넣어 가구용 및 인테리어용으로 사용할 수 있다는 효과가 얻어진다.As described above, according to the synthetic resin and wood according to the present invention for a furniture top plate and its manufacturing method, by forming a synthetic resin member between a pair of wood members can have aesthetic sense by wood and transparent synthetic resin, transparent or various The synthetic resin member having color can be integrally molded between the wooden members, and the effect that natural materials such as gravel and turban shells are put in the synthetic resin member can be used for furniture and interior.
본 발명에 따른 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법에 의하면, 합성수지부재를 소정의 두께로 성형한 다음 반복적으로 성형하여 목재부재와 동일한 높이로 형성할 수 있고, 목재부재 및 합성수지부재의 표면에 코팅 및 왁스 코팅을 하여 표면 광택에 의한 효과를 얻을 수 있으며, 종래의 목재 또는 합판으로 이루어진 가구용 상판관 동일하게 테이블, 문틀, 도어, 장롱, 싱크볼 등에도 자유롭게 사용할 수 있다는 효과가 얻어진다.According to the top plate for furniture using the synthetic resin and wood according to the present invention and its manufacturing method, the synthetic resin member is molded to a predetermined thickness and then repeatedly formed to form the same height as the wooden member, and the surface of the wooden member and the synthetic resin member The effect by surface gloss can be obtained by coating on and wax coating, and the effect that it can be used freely for tables, door frames, doors, cupboards, sink balls, etc. can be obtained in the same way as a conventional wood or plywood furniture top plate.
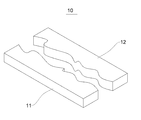
도 1은 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재를 도시한 입체도,
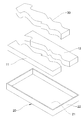
도 2는 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재와 이를 안착시키는 상판틀을 도시한 분해 입체도,
도 3은 본 발명의 바람직한 다른 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재와 이를 안착시키는 상판틀을 도시한 분해 입체도,
도 4는 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판을 도시한 입체도,
도 5는 본 발명의 바람직한 다른 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 상판틀을 도시한 평면도,
도 6은 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 제조공정을 도시한 공정도,
도 7은 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 제조방법에 의해 형성된 가구용 상판을 도시한 사진.1 is a three-dimensional view showing a wooden member of the top plate for furniture using a synthetic resin and wood according to a preferred embodiment of the present invention,
Figure 2 is an exploded three-dimensional view showing a wooden member of the top plate for furniture using a synthetic resin and wood in accordance with a preferred embodiment of the present invention and the seating frame therefor,
Figure 3 is an exploded three-dimensional view showing a wood member of the top plate for furniture and a top plate frame for seating it using a synthetic resin and wood according to another preferred embodiment of the present invention,
Figure 4 is a three-dimensional view showing a top plate for furniture using synthetic resin and wood according to a preferred embodiment of the present invention,
Figure 5 is a plan view showing a top plate of a furniture top plate using a synthetic resin and wood according to another preferred embodiment of the present invention,
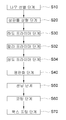
Figure 6 is a process diagram showing the manufacturing process of the top plate for furniture using a synthetic resin and wood according to a preferred embodiment of the present invention,
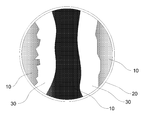
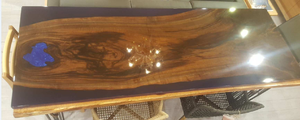
7 is a photograph showing a furniture top plate formed by a method for manufacturing a furniture top plate using synthetic resin and wood according to a preferred embodiment of the present invention.
이하 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판 및 그 제조방법을 첨부된 도면을 참조하여 상세하게 설명한다.Hereinafter, a top plate for furniture using synthetic resin and wood according to a preferred embodiment of the present invention and a method of manufacturing the same will be described in detail with reference to the accompanying drawings.
본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판은 소정의 높이 및 소정의 길이를 갖도록 목재를 소정의 길이로 절단하여 형성된 제1 목재부재(11)와 제2 목재부재(12), 소정의 간격만큼 이격된 상기 제1 목재부재(11)와 상기 제2 목재부재(12) 사이에 형성되는 합성수지부재(30)를 포함한다.The upper panel for furniture using synthetic resin and wood according to a preferred embodiment of the present invention is formed by cutting wood to a predetermined length so as to have a predetermined height and a predetermined length, a
본 발명의 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판은 소정의 거리만큼 이격된 제1 목재부재(11)와 제2 목재부재(12) 사이에 합성수지로 이루어진 합성수지부재(30)를 일체화시켜 줌으로써, 목재로 이루어진 테이블과 달리 합성수지부재(30)에 의해 내부가 외부로 투시되는 투명하게 이루어질 뿐만 아니라 소비자가 원하는 색상으로 이루어지며, 합성수지부재(30) 내부에 자갈, 소라 등의 천연소재가 외부로 투시되어 다양한 색상과 질감을 갖도록 한다.The top plate for furniture using synthetic resin and wood according to an embodiment of the present invention is obtained by integrating a
도 1은 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재를 도시한 입체도이고, 도 2는 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재와 이를 안착시키는 상판틀을 도시한 분해 입체도이다.1 is a three-dimensional view showing a wooden member of a top plate for furniture using synthetic resin and wood according to a preferred embodiment of the present invention, and FIG. 2 is a wooden member of a top plate for furniture using synthetic resin and wood according to a preferred embodiment of the present invention. It is an exploded three-dimensional view showing the upper frame for seating this.
도 1 및 도 2에 도시된 바와 같이, 본 발명의 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판은 좌우 양측에 구비되는 목재부재(10)와 상기 한 쌍의 목재부재(11, 12) 사이에 형성되는 합성수지부재(30)로 이루어진다.1 and 2, the top plate for furniture using synthetic resin and wood according to an embodiment of the present invention is provided between the
상기 목재부재(10)는 원목 등을 소정의 두께를 가짐은 물론 소정의 길이로 절단한다. 이러한 목재부재(10)는 2개로 이루어지는데, 제1 목재부재(11) 및 제2 목재부재(12)는 원목을 절단함에 따라 서로 다른 형상 및 모양으로 이루어진다.The
즉, 상기 제1 목재부재(11)와 제2 목재부재(12)는 서로 다른 형상과 모양을 갖게 된다.That is, the
이는 테이블 등으로 사용하고자 하는 경우에 해당되며, 목재부재(10)는 도어, 문틀, 장롱, 싱크대, 가구 등에 적용하고자 하는 경우 목재부재(10)인 제1 목재부재(11)와 제2 목재부재(12)를 동일한 크기 및 형상을 갖도록 형성될 수 있음은 물론이다.This corresponds to the case of using as a table, and the
상기 한 쌍의 목재부재(10)를 안정되게 안착시킬 수 있도록 상판틀(20)이 마련된다. 상기 상판틀(20)은 소정의 크기로 이루어진 바닥판(21)과 상기 바닥판(21)의 테두리에 소정 높이로 이루어진 측판(22)으로 이루어진다.The
상기 상판틀(20)의 바닥판(21)은 원목부재(10) 및 합성수지부재(30)의 크기에 따라 소정의 길이 및 폭으로 형성된다. 아울러 측판(22)은 제1 원목부재(11)와 제2 원목부재(12)를 안정되게 안착시켜 합성수지부재(30)의 성형 중에 제1 원목부재(11)와 제2 원목부재(12)가 움직이거나 이동되지 않게 고정시킨다.The
도 2에서 상판틀(20)은 사각형상으로 형성되어 있으나, 원형, 마름모형, 육각형 등의 다양한 형상으로 형성될 수 있음은 물론이다.In FIG. 2, the
이들 제1 원목부재(11)와 제2 원목부재(12) 사이에는 합성수지부재(30)가 성형된다. 상기 합성수지부재(30)는 에폭시, 레진 등의 합성수지를 총칭한다.A
상기 합성수지부재(30)는 자갈, 소라 등의 천연소재가 함침되며, 상기 합성수지부재(30)는 내부에 함침된 천연소재가 외부로 노출되도록 투명하게 형성되고, 상기 합성수지부재(30)의 색상이 다양한 색상 중 어느 하나로 이루어진다.The
상기 합성수지부재(30)는 투명하게 형성되거나 빨강, 노랑, 청색, 녹색 등의 다양한 색상으로 이루어지며, 이러한 합성수지부재(30)의 내부에 함침된 소재가 외부로 노출되게 형성된다.The
즉, 합성수지부재(30)는 내부가 들여다보이도록 형성되어 종래의 테이블과 달리 합성수지부재(30)에 의한 색상 및 투명하게 이루어져 합성수지부재(30)에 의한 심미감을 갖도록 한다.That is, the
도 3은 본 발명의 바람직한 다른 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 목재부재와 이를 안착시키는 상판틀을 도시한 분해 입체도이다.Figure 3 is an exploded three-dimensional view showing a wood member of the top plate for furniture and a top plate for mounting it using a synthetic resin and wood according to another preferred embodiment of the present invention.
도 3은 본 발명의 다른 실시 예를 도시한 것으로, 가구용 상판의 표면에 유리판(25)을 일체로 구비되게 한다.Figure 3 shows another embodiment of the present invention, to be integrally provided with a
즉, 상기 바닥판(21)의 상면에는 유리판(25)을 안착시킴과 함께 상기 유리판(25)의 상면에 제1 목재부재(11)와 제2 목재부재(12)를 서로 이격되게 안착시킨다.That is, the
이와 같이 유리판(25)의 상면에는 합성수지부재(30)를 목재부재(10) 사이에 성형함으로써, 목재부재(10), 유리판(25) 및 합성수지부재(30)를 일체화시킨다.Thus, by forming the
도 4는 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판을 도시한 입체도이다.4 is a three-dimensional view showing a top plate for furniture using synthetic resin and wood according to a preferred embodiment of the present invention.
도 4에 도시된 바와 같이, 본 발명의 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판은 한 쌍의 목재부재(11, 12) 사이에 합성수지부재(30)가 일체로 이루어져 가구용 상판으로 사용된다.As shown in FIG. 4, the synthetic resin and wood upper plate for furniture according to an embodiment of the present invention are used as a furniture upper plate, as a
도 5는 본 발명의 다른 실시 예에 따른 상판틀(20)을 도시한 것으로, 상기 상판틀(20)은 원형으로 이루어지며, 상기 원형의 상판틀(20) 내부에는 일정 간격으로 이격된 다수의 목재부재(10)를 안착시킨다.Figure 5 shows the
도 5에서와 같이, 상기 상판틀(20) 내부에는 서로 다른 형상의 모양을 갖는 3개의 목재부재(10)를 안착시킨 다음 이들 목재부재(10)에 의해 빈 공간에 합성수지를 채워 합성수지부재(30)를 형성하게 된다.As shown in FIG. 5, three
본 발명의 실시 예에 따른 가구용 상판은 한 쌍의 목재부재(10) 사이에 합성수지부재(30)가 일체화되어 목재부재(10)와 합성수지부재(30)에 의해 테이블, 문틀, 도어, 장롱, 싱크대 등의 가구 또는 인테리어용으로 사용된다.The top plate for furniture according to an embodiment of the present invention is a
도 6은 본 발명의 바람직한 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 제조방법법을 단계별로 설명하는 공정도이다.6 is a process diagram for explaining step-by-step a method of manufacturing a furniture top using a synthetic resin and wood according to a preferred embodiment of the present invention.
본 발명의 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 제조방법은 (a) 목재부재를 선별하는 단계; (b) 선별된 목재부재 중 한 쌍의 상기 목재부재를 상판틀의 양 측면에 밀착시켜 이격된 한 쌍의 목재부재 사이에 합성수지부재가 성형되도록 안착시키는 단계; (c) 상기 한 쌍의 목재부재 사이에 합성수지를 부어 소정의 두께로 경화시키는 하도 프라이머 성형 단계; (d) 상기 하도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 중도 프라이머 성형 단계; (e) 상기 중도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 상도 프라이머 성형 단계; (f) 상기 한 쌍의 목재부재 및 상기 프라이머에 의해 형성된 합성수지부재의 상면을 고르게 평판화시키는 단계; (g) 상기 한 쌍의 목재부재 및 상기 합성수지부재로 이루어진 가구용 상판의 표면을 샌딩하는 단계; (h) 상기 가구용 상판의 표면에 소정의 두께로 코팅하는 단계; (i) 상기 가구용 상판의 코팅면에 왁스를 코팅하는 단계;를 포함한다.A method of manufacturing a top plate for furniture using synthetic resin and wood according to an embodiment of the present invention includes: (a) selecting a wooden member; (B) step of placing a pair of the wood member of the selected wood member in close contact with both sides of the upper frame to form a synthetic resin member between the spaced pair of wood members; (C) primer forming step of the primer to pour a synthetic resin between the pair of wood members to a predetermined thickness; (d) a middle primer molding step of pouring a synthetic resin on the primer to cure to a predetermined thickness; (e) a top primer forming step of pouring a synthetic resin on the middle primer to cure to a predetermined thickness; (f) evenly flattening the upper surfaces of the pair of wood members and the synthetic resin member formed by the primer; (g) sanding the surface of the top plate for furniture made of the pair of wooden members and the synthetic resin member; (h) coating the surface of the furniture top plate with a predetermined thickness; (i) coating the wax on the coating surface of the furniture top plate; includes.
도 1 내지 도 6에 도시된 바와 같이, 본 발명의 실시 예에 따른 합성수지와 목재를 이용한 가구용 상판의 제조방법은 제1 목재부재(11)와 제2 목재부재(12)를 선별한다(S10).1 to 6, the method of manufacturing a top plate for furniture using synthetic resin and wood according to an embodiment of the present invention sorts the
이러한 목재부재(10)의 선별은 제작하고자 하는 가구용 상판의 종류에 따라 적절한 목재를 선별하게 된다. 즉, 가구용 상판을 테이블로 사용하고자 하는 경우, 원목을 소정의 두께 및 길이로 커팅하여 한 쌍의 목재부재(10)를 마련한다.The selection of the
또 가구용 상판을 도어로 사용하고자 하는 경우, 원목 또는 합판 등을 소정의 두께 및 길이로 커팅한다. 이때 원목 또는 합판은 상판틀(20)의 측판(22)에 밀착되도록 일직선상으로 커팅한다.In addition, when a top plate for furniture is to be used as a door, wood or plywood is cut to a predetermined thickness and length. At this time, the wood or plywood is cut in a straight line so as to be in close contact with the
아울러 선별된 목재부재는 상판틀(20)의 내부에 안착시킨다(S20).In addition, the selected wooden member is seated inside the top plate frame 20 (S20).
상기 상판틀(20)은 사각 형상으로 이루어진 바닥판(21)의 가장자리에 각각 측판(22)을 고정하며, 합성수지부재(30)의 성형에 따라 합성수지가 상판틀(20)의 외부로 누출되지 않도록 열가소성 플라스틱 접착제를 도포한다.The
즉, 글루 건(Glue Gun)을 이용하여 열가소성 플라스틱 접착제를 도포하여 바닥판(21)과 측판(22) 사이를 밀폐시킨다.That is, a thermoplastic plastic adhesive is applied using a glue gun to seal between the
이와 같은 상판틀(20)의 내부에는 선별된 목재부재(10)를 안착시키는데, 상기 목재부재(10)의 일직선으로 이루어진 제1 목재부재(11)의 일면을 측판(22)에 밀착시킨다.The selected
아울러 상판틀(20)의 내부에는 제2 목재부재(12)의 일면을 다른 측판(22)에 밀착시키며, 상기 제1 목재부재(11)와 제2 목재부재(12)는 상판틀(20)의 내부에 소정의 거리만큼 이격되게 안착된다.In addition, the inside of the
한편 필요에 따라 목재부재(10)의 저면에는 유리판(25)을 안착시킨 다음에 유리판(25)의 상면에 목재부재(10)를 안착시킬 수 있다. 이는 유리판(25)을 합성수지부재(30)에 일체화시켜 유리 및 투명한 합성수지부재(30)에 의해 다양한 형태의 가구용 상판을 제작할 수 있도록 하기 위함이다.On the other hand, if necessary, the
상기 프라이머 성형 단계는 상기 한 쌍의 목재부재(11, 12) 사이에 소정 두께로 합성수지를 부어 경화시키는 하도 프라이머 성형 단계(S30), 상기 하도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 중도 프라이머 성형 단계(S32), 상기 중도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 상도 프라이머 성형 단계(S34)를 포함한다.The primer forming step is a primer primer forming step (S30) of pouring a synthetic resin to a predetermined thickness between the pair of
상기 제1 목재부재(11)와 제2 목재부재(12) 사이에는 합성수지를 부어 소정의 두께로 하도 프라이머를 경화시킨다(S30).A synthetic resin is poured between the
상기 합성수지는 에폭시 프라이머로써, 주제인 에폭시와 경화제를 대략 3:1의 비율로 혼합하여 제1 목재부재(11)와 제2 목재부재(12) 사이에 부어 경화시킨다.The synthetic resin is an epoxy primer, and the main epoxy and a curing agent are mixed at a ratio of approximately 3: 1 to pour and cure between the
이러한 하도 프라이머 성형 단계에서 프라이머는 대략 0.5㎜의 두께로 형성하며, 하도 프라이머가 경화된 다음에 재차 프라이머를 0.5㎜의 두께로 부어 경화시킨다.In this primer forming step, the primer is formed to a thickness of approximately 0.5 mm, and after the primer is cured, the primer is again poured to a thickness of 0.5 mm to cure.
이와 같이 프라이머를 0.5㎜의 두께로 부어 경화시키는 과정을 다수 반복하여 소정의 두께로 형성하며, 이때 프라이머는 투명 에폭시 프라이머를 사용하여 합성수지부재(30)의 내부가 외부로 노출되게 한다.As described above, a process of pouring and curing the primer with a thickness of 0.5 mm is repeated to form a predetermined thickness, and the primer is made of a transparent epoxy primer to expose the inside of the
이어서 하도 프라이머가 경화되면, 자갈, 소라 등의 천연소재 등을 합성수지부재(30) 내부에 안착시킨다. 상기 하도 프라이머 상에는 투명한 프라이머 또는 색상을 갖는 프라이머를 0.5㎜의 두께로 부어 경화시켜 칼라 프라이머를 성형한다(S32).Subsequently, when the primer is cured, natural materials such as gravel and conch are placed inside the
이때 색상을 갖는 프라이머는 에폭시: 칼라에폭시: 경화제를 3:3:1의 비율로 혼합하여 원하는 색상의 프라이머를 준비한다. 아울러 칼라 프라이머는 0.5㎜의 두께로 성형되는데, 하도 프라이머와 같이 칼라 프라이머를 반복적으로 성형한다.At this time, a primer having a color is prepared by mixing an epoxy: color epoxy: curing agent in a ratio of 3: 3: 1 to prepare a primer of a desired color. In addition, the color primer is formed to a thickness of 0.5 mm, and the color primer is repeatedly molded like a primer.
또한 칼라 프라이머가 경화되면, 에폭시와 경화제가 혼합된 프라이머를 칼라 프라이머의 상면에 0.5㎜의 두께로 부어 경화시킨다(S34).In addition, when the color primer is cured, a primer mixed with an epoxy and a curing agent is cured by pouring it to a thickness of 0.5 mm on the top surface of the color primer (S34).
상기 프라이머 성형 단계는 프라이머를 소정 두께로 부어 경화시킨 다음 재차 프라이머를 부어 소정 두께로 경화시키는 과정이 반복적으로 이루어진다.In the primer forming step, the primer is poured into a predetermined thickness to cure, and then the primer is poured again to cure to a predetermined thickness repeatedly.
아울러 합성수지부재(30)는 목재부재(10)의 높이와 동일하게 성형되며, 이에 제1 목재부재(11)와 제2 목재부재(12) 사이에는 합성수지부재(30)가 일체로 성형된 상태에서 상판틀(20)로부터 분리시켜 꺼내게 된다.In addition, the
상기 합성수지부재(30)는 가구용 상판의 표면으로 사용하고자 하는 면을 평판화시킨다(S40).The
상기 평판화 단계는 CNC 또는 루퍼 등의 기계를 이용하여 목재부재(10), 합성수지부재(30)의 표면을 평활하게 한다. 아울러 가구용 상판의 상면 및 측면을 평활하게 하며, 이후 샌딩 단계에서 광택작업이 원활하게 이루어지도록 하기 위함이다.The flattening step smooths the surfaces of the
상기 목재부재(10) 및 합성수지부재(30)로 이루어진 가구용 상판은 표면의 거칠기를 매끈하도록 샌딩한다(S50).The upper surface for furniture made of the
이러한 샌딩 작업은 사포의 320방에서부터 순차적으로 5000방으로 보다 작은 입자를 갖는 사포로 샌딩하게 된다.This sanding operation is sanding with sandpaper having smaller particles from 320 rooms of sandpaper to 5000 rooms sequentially.
이어서 가구용 상판은 황변현상 및 스크래치가 발생되지 않도록 하이브리드 에폭시를 스프레이 작업에 의해 나노 코팅을 한다(S60).Subsequently, the furniture top plate is nano-coated by spraying a hybrid epoxy to prevent yellowing and scratching (S60).
즉, 가구용 상판은 장기간 사용 중에 합성수지부재(30)의 색상이 변하지 않도록 함은 물론 합성수지부재(30)의 표면에 스크래치 등이 발생되지 않도록 나노 코팅이 이루어지게 된다.That is, the top plate for furniture is nano-coated so that the color of the
이러한 나노 코팅은 하이브리드 에폭시를 스프레이로 고르게 분사하여 가구용 상판의 표면에 도포한다.The nano coating is applied evenly to the surface of the furniture top plate by spraying the hybrid epoxy evenly with a spray.
이어서 가구용 상판의 표면에는 왁스를 코팅한다(S70).Subsequently, a wax is coated on the surface of the top plate for furniture (S70).
이러한 왁스 코팅은 가구용 상판의 표면에 광택을 내기 위한 것으로, 왁스를 소정량으로 바른 다음 문질러서 코팅을 하게 된다.The wax coating is intended to give a gloss to the surface of the furniture top plate, and is coated with a predetermined amount of wax and then rubbed.
도 7은 본 발명의 가구용 상판의 제조방법에 의해 형성된 가구용 상판을 도시한 것으로, 투명 또는 색상을 갖는 투명한 색으로 합성수지부재(30)가 목재부재(10)의 외측에 일체로 성형된다.7 shows a furniture top plate formed by a method for manufacturing a furniture top plate according to the present invention, the
이상 본 발명자에 의해서 이루어진 발명을 상기 실시 예에 따라 구체적으로 설명하였지만, 본 발명은 상기 실시 예에 한정되는 것은 아니고 그 요지를 이탈하지 않는 범위에서 여러 가지로 변경 가능한 것은 물론이다.Although the invention made by the present inventors has been described in detail according to the above-described embodiments, the present invention is not limited to the above-described embodiments and can be variously changed within a range not departing from the gist thereof.
10: 목재부재 11: 제1 목재부재
12: 제2 목재부재
20: 상판틀 21: 바닥판
22: 측판 25: 유리판
30: 합성수지부재10: wood member 11: first wood member
12: second wooden member
20: top frame 21: bottom plate
22: side plate 25: glass plate
30: synthetic resin member
Claims (6)
소정의 간격만큼 이격된 상기 제1 목재부재와 상기 제2 목재부재 사이에 형성되는 합성수지부재;를 포함하는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판.A first wood member and a second wood member formed by cutting wood to a predetermined length so as to have a predetermined height and a predetermined length;
And a synthetic resin member formed between the first wood member and the second wood member spaced apart by a predetermined interval.
상기 합성수지부재는 자갈, 소라 등의 천연소재가 함침되며,
상기 합성수지부재는 내부에 함침된 천연소재가 외부로 노출되도록 투명하게 형성되고, 상기 합성수지부재의 색상이 다양한 색상 중 어느 하나로 이루어지는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판.According to claim 1,
The synthetic resin member is impregnated with natural materials such as gravel and turban,
The synthetic resin member is transparently formed so that the natural material impregnated therein is exposed to the outside, and the color of the synthetic resin member is made of any one of various colors.
(b) 선별된 목재부재 중 한 쌍의 상기 목재부재를 상판틀의 양 측면에 밀착시켜 이격된 한 쌍의 목재부재 사이에 합성수지부재가 성형되도록 안착시키는 단계;
(c) 상기 한 쌍의 목재부재 사이에 소정 두께로 합성수지를 부어 경화시키는 과정을 반복적으로 하여 상기 한 쌍의 목재부재 사이에 상기 목재부재와 동일한 높이로 합성수지부재를 성형하는 단계;
(d) 상기 한 쌍의 목재부재 및 상기 프라이머에 의해 형성된 합성수지부재의 상면을 고르게 평판화시키는 단계;
(e) 상기 한 쌍의 목재부재 및 상기 합성수지부재로 이루어진 가구용 상판의 표면을 샌딩하는 단계;
(f) 상기 가구용 상판의 표면에 소정의 두께로 코팅하는 단계;
(g) 상기 가구용 상판의 코팅면에 왁스를 코팅하는 단계;를 포함하는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판의 제조방법.(A) selecting a wooden member;
(B) step of placing a pair of the wood member of the selected wood member in close contact with both sides of the upper frame to form a synthetic resin member between the spaced pair of wood members;
(c) forming a synthetic resin member at the same height as the wooden member between the pair of wooden members by repeatedly performing a process of pouring and curing a synthetic resin with a predetermined thickness between the pair of wooden members;
(d) evenly flattening the upper surfaces of the pair of wood members and the synthetic resin member formed by the primer;
(E) sanding the surface of the top plate for furniture made of the pair of wood members and the synthetic resin member;
(f) coating the surface of the furniture top plate with a predetermined thickness;
(g) coating the wax on the coated surface of the furniture top plate; a method for manufacturing a furniture top plate using synthetic resin and wood, comprising a.
상기 (c) 단게에서, (c1) 상기 한 쌍의 목재부재 사이에 소정 두께로 합성수지를 부어 경화시키는 하도 프라이머 성형 단계;
(c2) 상기 하도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 중도 프라이머 성형 단계;
(c3) 상기 중도 프라이머 상에 합성수지를 부어 소정 두께로 경화시키는 상도 프라이머 성형 단계;를 포함하는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판의 제조방법.According to claim 3,
In the step (c), (c1) primer primer forming step of curing by pouring a synthetic resin to a predetermined thickness between the pair of wood members;
(c2) a middle primer forming step of pouring a synthetic resin on the primer to cure to a predetermined thickness;
(c3) a top coat primer forming step of pouring a synthetic resin on the intermediate primer to cure to a predetermined thickness; a method for manufacturing a top plate for furniture using synthetic resin and wood.
상기 (c) 단계에서, 상기 프라이머 성형 단계는 프라이머를 소정 두께로 부어 경화시킨 다음 재차 프라이머를 부어 소정 두께로 경화시키는 과정이 반복적으로 이루어지는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판의 제조방법.The method of claim 4,
In the step (c), the primer forming step is a method of manufacturing a top plate for furniture using synthetic resin and wood, characterized in that the primer is poured into a predetermined thickness to cure and then the primer is poured again to cure to a predetermined thickness.
상기 (f) 단계에서, 상기 합성수지부재의 황변현상 및 스크래치가 발생되지 않도록 하이브리드 에폭시를 스프레이 작업에 의해 나노 코팅이 이루어지는 것을 특징으로 하는 합성수지와 목재를 이용한 가구용 상판의 제조방법.According to claim 3,
In the step (f), a method for manufacturing a furniture top plate using synthetic resin and wood, characterized in that nano-coating is performed by spraying a hybrid epoxy to prevent yellowing and scratching of the synthetic resin member.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020180140604A KR20200056661A (en) | 2018-11-15 | 2018-11-15 | Furniture Top Plate using Synthetic Resin and Wood and Manufacturing Method Thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020180140604A KR20200056661A (en) | 2018-11-15 | 2018-11-15 | Furniture Top Plate using Synthetic Resin and Wood and Manufacturing Method Thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| KR20200056661A true KR20200056661A (en) | 2020-05-25 |
Family
ID=70914435
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| KR1020180140604A Ceased KR20200056661A (en) | 2018-11-15 | 2018-11-15 | Furniture Top Plate using Synthetic Resin and Wood and Manufacturing Method Thereof |
Country Status (1)
| Country | Link |
|---|---|
| KR (1) | KR20200056661A (en) |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20120006621U (en) | 2011-03-17 | 2012-09-26 | 정용희 | Top panel of furniture |
| KR101735070B1 (en) | 2016-12-21 | 2017-05-15 | 주식회사 마이바움 | Prefabricated roofing for furniture |
-
2018
- 2018-11-15 KR KR1020180140604A patent/KR20200056661A/en not_active Ceased
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20120006621U (en) | 2011-03-17 | 2012-09-26 | 정용희 | Top panel of furniture |
| KR101735070B1 (en) | 2016-12-21 | 2017-05-15 | 주식회사 마이바움 | Prefabricated roofing for furniture |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| RU2257998C2 (en) | Reverse molding panel | |
| US10603812B2 (en) | Process of making compreg multi-colored laminated wood and utility, ornamental, decorative products thereof | |
| CA2293141C (en) | Method for making corners for laminate and veneer countertops | |
| US20150140281A1 (en) | Nestable molded articles, and related assemblies and methods | |
| US7960004B2 (en) | Glue-laminated bamboo furniture | |
| WO1998023422A1 (en) | A method for the manufacture of a curved wooden fibre plate and a wooden fibre plate manufactured hereby | |
| KR20190112349A (en) | The assembling structure for a furniture | |
| KR102375956B1 (en) | Furniture plate with antibacterial effect and furniture using the same | |
| US7481900B1 (en) | Method of manufacturing a molded door skin | |
| KR101916521B1 (en) | Composite panel and manufacturing method the same | |
| CA2420761A1 (en) | Seamless door and methods of manufacture | |
| US4535019A (en) | Laminated wood coupling arrangement | |
| US8226788B1 (en) | Method of manufacturing a molded door | |
| KR200345225Y1 (en) | A functional interior board | |
| CN212394362U (en) | Decorative surface of complete furniture | |
| CN110303567A (en) | The method for manufacturing solid wooden compound floor | |
| CN204023969U (en) | A kind of composite floor | |
| KR20080091935A (en) | Kitchen and interior doors and how to make them | |
| KR200374083Y1 (en) | Bamboo floor-board | |
| RU2294843C2 (en) | Method of producing wood articles with amber incrustation | |
| JPH06146552A (en) | Floor board | |
| KR100545364B1 (en) | Method for manufacturing solid wood panel and solid wood panel produced by this method | |
| JP3243447U (en) | Decorative table with Kumiko style | |
| Crow | Mid-Century Modern Furniture: Shop Drawings & Techniques for Making 29 Projects | |
| GB2101523A (en) | Laminar objects and method of construction |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PA0109 | Patent application |
St.27 status event code: A-0-1-A10-A12-nap-PA0109 |
|
| PA0201 | Request for examination |
St.27 status event code: A-1-2-D10-D11-exm-PA0201 |
|
| PA0302 | Request for accelerated examination |
St.27 status event code: A-1-2-D10-D17-exm-PA0302 St.27 status event code: A-1-2-D10-D16-exm-PA0302 |
|
| D13-X000 | Search requested |
St.27 status event code: A-1-2-D10-D13-srh-X000 |
|
| D14-X000 | Search report completed |
St.27 status event code: A-1-2-D10-D14-srh-X000 |
|
| PE0902 | Notice of grounds for rejection |
St.27 status event code: A-1-2-D10-D21-exm-PE0902 |
|
| E13-X000 | Pre-grant limitation requested |
St.27 status event code: A-2-3-E10-E13-lim-X000 |
|
| P11-X000 | Amendment of application requested |
St.27 status event code: A-2-2-P10-P11-nap-X000 |
|
| P13-X000 | Application amended |
St.27 status event code: A-2-2-P10-P13-nap-X000 |
|
| PE0601 | Decision on rejection of patent |
St.27 status event code: N-2-6-B10-B15-exm-PE0601 |
|
| E13-X000 | Pre-grant limitation requested |
St.27 status event code: A-2-3-E10-E13-lim-X000 |
|
| P11-X000 | Amendment of application requested |
St.27 status event code: A-2-2-P10-P11-nap-X000 |
|
| P13-X000 | Application amended |
St.27 status event code: A-2-2-P10-P13-nap-X000 |
|
| PX0901 | Re-examination |
St.27 status event code: A-2-3-E10-E12-rex-PX0901 |
|
| PX0601 | Decision of rejection after re-examination |
St.27 status event code: N-2-6-B10-B17-rex-PX0601 |
|
| PJ0201 | Trial against decision of rejection |
St.27 status event code: A-3-3-V10-V11-apl-PJ0201 |
|
| PG1501 | Laying open of application |
St.27 status event code: A-1-1-Q10-Q12-nap-PG1501 |
|
| J301 | Trial decision |
Free format text: TRIAL NUMBER: 2019101003703; TRIAL DECISION FOR APPEAL AGAINST DECISION TO DECLINE REFUSAL REQUESTED 20191107 Effective date: 20201029 |
|
| PJ1301 | Trial decision |
St.27 status event code: A-3-3-V10-V15-crt-PJ1301 Decision date: 20201029 Appeal event data comment text: Appeal Kind Category : Appeal against decision to decline refusal, Appeal Ground Text : 2018 0140604 Appeal request date: 20191107 Appellate body name: Patent Examination Board Decision authority category: Office appeal board Decision identifier: 2019101003703 |
|
| P22-X000 | Classification modified |
St.27 status event code: A-2-2-P10-P22-nap-X000 |
|
| R18-X000 | Changes to party contact information recorded |
St.27 status event code: A-3-3-R10-R18-oth-X000 |
|
| R18 | Changes to party contact information recorded |
Free format text: ST27 STATUS EVENT CODE: A-3-3-R10-R18-OTH-X000 (AS PROVIDED BY THE NATIONAL OFFICE) |
|
| R18-X000 | Changes to party contact information recorded |
St.27 status event code: A-3-3-R10-R18-oth-X000 |