JP5404019B2 - Recycling method for waste aluminum products - Google Patents
Recycling method for waste aluminum products Download PDFInfo
- Publication number
- JP5404019B2 JP5404019B2 JP2008318969A JP2008318969A JP5404019B2 JP 5404019 B2 JP5404019 B2 JP 5404019B2 JP 2008318969 A JP2008318969 A JP 2008318969A JP 2008318969 A JP2008318969 A JP 2008318969A JP 5404019 B2 JP5404019 B2 JP 5404019B2
- Authority
- JP
- Japan
- Prior art keywords
- aluminum
- waste
- waste aluminum
- recycling
- heat treatment
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images
Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P10/00—Technologies related to metal processing
- Y02P10/20—Recycling
Landscapes
- Processing Of Solid Wastes (AREA)
- Manufacture And Refinement Of Metals (AREA)
Description
本発明は、廃棄アルミ製品のリサイクル処理方法に関し、特に使用済みのアルミ缶を対象にして製鋼用副原料(例えば脱酸材)として又はアルミニウム二次合金の主原料として再利用するために好適に用いられるリサイクル処理方法に関する。 The present invention relates to a recycling method for waste aluminum products, and is particularly suitable for reuse as a secondary material for steel making (for example, a deoxidizing material) or as a main raw material for an aluminum secondary alloy for used aluminum cans. It relates to the recycling method used.
従来、使用済み飲料缶を回収してリサイクルする技術として種々のものが提案されている。例えば使用済みのアルミ缶をアルミ缶用板材の溶解原料として再利用するための処理方法として、アルミ缶を破砕機で裁断し、裁断したアルミ片をロータリーキルンに入れて550℃〜600℃で焼成して表面塗装等を燃焼・除去した後に、インパクトミルに入れて高速回転している打撃板や反発板に落下して衝突することを反復繰り返させてアルミペレット(アルミ小球状塊)に成形し、サイズが大きければアルミペレットのまま、小さければアルミペレットを集めてブリケットマシンに入れてより大きなアルミ塊に成形して再利用する、というものが提案されている(例えば特許文献1参照)。 Conventionally, various techniques for collecting and recycling used beverage cans have been proposed. For example, as a treatment method for reusing used aluminum cans as a raw material for dissolving aluminum can plates, the aluminum cans are cut with a crusher, and the cut aluminum pieces are placed in a rotary kiln and fired at 550 ° C to 600 ° C. After burning and removing the surface coating, etc., it is put into an impact mill and repeatedly hitting and colliding with a striking plate or repulsion plate rotating at high speed, and forming into aluminum pellets (aluminum small spherical lump), It has been proposed that aluminum pellets remain as they are when the size is large, and are collected into a briquette machine and formed into a larger aluminum lump for reuse (see, for example, Patent Document 1).
又、使用済みのスチール缶とアルミ缶とが混在した状態のものからスチールペレットとアルミペレットに分離して再利用するための処理方法として、混在状態の飲料缶を裁断機で細かく裁断した上で、ロータリーキルンに入れて450℃〜500℃に加熱し、加熱後に磁選機によりスチール断片とアルミ断片とに分離して、分離したアルミ断片を造粒機でアルミペレットに成形する、というものも提案されている(例えば特許文献2参照)。 In addition, as a treatment method for separating and reusing steel pellets and aluminum pellets from a mixture of used steel cans and aluminum cans, the mixed beverage cans can be cut into pieces with a cutting machine. It is also proposed to put in a rotary kiln, heat to 450 ° C to 500 ° C, separate into steel pieces and aluminum pieces with a magnetic separator after heating, and form the separated aluminum pieces into aluminum pellets with a granulator (For example, refer to Patent Document 2).
さらに、使用済みのスチール缶から蓋部分のアルミニウム材料と胴部分のスチール材料とを別々に取り出して再利用するための処理方法として、スチール缶をインパクトクラッシャーで破砕した上で、その破砕した断片をロータリーキルンで加熱して表面塗装等を燃焼・除去し、加熱後のスチール材料とアルミ材料との各断片を粗造粒機・造粒機の2段式によりスチールペレットとアルミペレットの粒状に加工・成形した後に、磁選機でスチールペレットとアルミペレットとに分離する、というものが提案されている(例えば特許文献3参照)。 Furthermore, as a processing method for taking out the aluminum material of the lid part and the steel material of the trunk part separately from the used steel can and reusing them, the steel can is crushed with an impact crusher, and then the crushed pieces are removed. Heating with a rotary kiln to burn and remove surface coating, etc., and processing each piece of steel material and aluminum material after heating into steel pellets and aluminum pellets by a two-stage system of coarse granulator and granulator There has been proposed a method of separating into steel pellets and aluminum pellets using a magnetic separator after molding (see, for example, Patent Document 3).
ところが、従来の廃棄アルミ製品のリサイクル処理方法においては、いずれも再利用するためにアルミペレットという粒状の形態に造粒するようにしており、このペレット化(造粒化)に起因して種々の不都合が生じている。なお、本件における「造粒」は、粉体を造粒・固化させてペレットを形成するという場合の通常の「造粒」技術とは異なり、加熱により軟らかくなったアルミ片を主として衝撃力・打撃力により粒状の形態に成形するという技術に係るものである。 However, in the conventional recycling methods for waste aluminum products, all of them are granulated into a granular form called aluminum pellets for reuse. There is an inconvenience. Note that “granulation” in this case is different from the usual “granulation” technology in which powder is granulated and solidified to form pellets. It relates to a technique of forming into a granular form by force.
すなわち、上記不都合として、ペレット化するために用いる造粒機の損耗が激しく機能維持のためのランニングコストの増大化を招く上に、駆動のために多大な電力エネルギーの消費を余儀なくされている、という点がある。すなわち、造粒機の連続運転により特にスクリーンの穴が損耗して徐々に潰れていき、この結果、ペレット形状の不均一化・小サイズ化や破砕粉の増加を招き、メンテナンスや部品交換頻度の増大や歩留まり悪化を招くことになる。このため、使用済みアルミ缶を資源として再利用するという事業を確立する上で、障害になっている。 That is, as the above inconvenience, the granulator used for pelletization is heavily worn, leading to an increase in running cost for maintaining the function, and a great amount of power energy is forced to drive, There is a point. In other words, the continuous operation of the granulator causes the holes in the screen to wear out and gradually collapse, resulting in non-uniform pellet size, an increase in the size of crushed powder, and maintenance and parts replacement frequency. This will cause an increase and a decrease in yield. For this reason, it has become an obstacle to establishing a business of reusing used aluminum cans as resources.
加えて、アルミペレットは比重が軽すぎて、製鋼用副原料として再利用するには使い難いという点がある。すなわち、最終溶解炉に投入する際の搬送コンベアから落下したりこぼれたりして最終溶解量の歩留まりの悪化を招いたり、最終溶解炉に投入する際に吹き上がって炉内下部まで到達しないものがあったりする。 In addition, the specific gravity of aluminum pellets is so low that it is difficult to reuse as an auxiliary material for steelmaking. That is, there are things that fall from the conveyor when thrown into the final melting furnace and cause the yield of the final melting amount to deteriorate, or those that blow up when reaching the final melting furnace and do not reach the lower part of the furnace There is.
又、使用済みアルミ缶を対象にしてリサイクル処理を実施する場合、その使用済みアルミ缶を加熱前に裁断しても、スチール製の異物の選別・除去はともかくとして、スチール製以外の異物の選別・除去がかえって困難となり易くなり、異物混入のままアルミペレットに成形されてアルミニウムの純度の著しい低下を招くおそれがある。 When recycling used aluminum cans, even if the used aluminum cans are cut before heating, it is possible to sort out non-steel foreign matter, regardless of the sorting and removal of steel foreign matter. -Removal tends to be difficult, and may be formed into aluminum pellets with foreign matter mixed in, resulting in a significant decrease in the purity of aluminum.
本発明は、このような事情に鑑みてなされたものであり、その目的とするところは、造粒工程を省略して高比重、高純度の再利用可能な原料が得られる廃棄アルミ製品のリサイクル処理方法を提供することにある。 The present invention has been made in view of such circumstances, and its purpose is to recycle waste aluminum products that can omit a granulation step and obtain a recyclable raw material with high specific gravity and high purity. It is to provide a processing method.
上記目的を達成するために、本発明では、廃棄アルミ製品のリサイクル処理方法を対象にして、廃棄アルミ製品を還元雰囲気にした加熱炉内において焼成温度条件でかつ酸化を防止し得る温度条件となる所定温度範囲で乾留させる加熱処理工程と、加熱処理工程後に破砕・裁断してアルミ細片にする破砕処理工程と、破砕処理工程後のアルミ細片を圧縮固化させてアルミブリケットに成型するブリケット成型工程とを備えることとした。ここで、上記の所定温度範囲としては400℃〜500℃、中でも400℃〜450℃が好ましいものとして挙げられる。 In order to achieve the above object, the present invention targets a recycling method for waste aluminum products, and is a temperature condition capable of preventing oxidation in a heating furnace in which the waste aluminum product is in a reducing atmosphere. A heat treatment process for dry distillation in a predetermined temperature range, a crushing process for crushing and cutting into aluminum pieces after the heat treatment process, and a briquette molding for compressing and solidifying the aluminum pieces after the crushing treatment process to form aluminum briquettes A process. Here, as said predetermined temperature range, 400 degreeC-500 degreeC, Especially 400 degreeC-450 degreeC are mentioned as a preferable thing.
この特定事項の場合、加熱処理工程により、廃棄アルミ製品を酸化させることなく表面処理された塗料やコーティング材、あるいは、表面に付着した水分や不純物を熱分解させることが可能となり、これにより、廃棄アルミ製品から本来の素材であるアルミニウム合金以外の不純物を除去すると共に、焼き鈍すことが可能になる。次に、破砕工程において、焼き鈍された加熱処理後の廃棄アルミ製品が破砕・裁断されてアルミ細片にされ、このアルミ細片がブリケット成形工程で圧縮固化されて高比重・高純度のアルミブリケットが得られることになる。このアルミブリケットが脱酸材等の製鋼用副原料又は新たなアルミ製品の原料等として再利用されることになる。加えて、特に、加熱処理工程において、密閉可能な加熱炉と、循環ファンと、加熱ガス発生室とを用い、循環ファンの作動により上記加熱炉での加熱により生成された熱分解ガスを加熱ガス発生室に循環供給し、この加熱ガス発生室で熱分解ガスを燃焼させることにより発生する燃焼排ガスを上記加熱炉に対し還元雰囲気で乾留させる加熱源として供給するようにした(請求項1)。この場合、加熱炉での乾留により生成される熱分解ガスが加熱ガス発生室において燃焼されその燃焼排ガスが加熱炉に戻されることで、加熱処理工程における還元雰囲気での加熱処理が確実に行われることになる。 In the case of this specific matter, the heat treatment process makes it possible to thermally decompose the surface-treated paints and coating materials, or moisture and impurities adhering to the surface without oxidizing the waste aluminum product. Impurities other than the aluminum alloy, which is the original material, can be removed from the aluminum product and annealed. Next, in the crushing process, the annealed waste aluminum product after heat treatment is crushed and cut into aluminum strips, and the aluminum strips are compressed and solidified in the briquette forming process to produce high specific gravity and high purity aluminum. Briquette will be obtained. This aluminum briquette is reused as a secondary material for steel making such as a deoxidizing material or a raw material for a new aluminum product. In addition, in particular, in the heat treatment process, a heat-sealable heating furnace, a circulation fan, and a heating gas generation chamber are used. Circulation supply to the generation chamber is performed, and combustion exhaust gas generated by burning pyrolysis gas in the heating gas generation chamber is supplied to the heating furnace as a heating source for dry distillation in a reducing atmosphere (claim 1). In this case, the pyrolysis gas generated by dry distillation in the heating furnace is combusted in the heating gas generation chamber, and the combustion exhaust gas is returned to the heating furnace, so that the heat treatment in the reducing atmosphere in the heat treatment process is reliably performed. It will be.
この発明において、多数の廃棄アルミ製品が矩形形状に軽圧縮成形された状態のプレススクラップを出発原料にする場合、このプレススクラップを軽圧縮成形状態から解放して個々の廃棄アルミ製品に分離する解放工程と、個々に分離された状態の廃棄アルミ製品からこの廃棄アルミ製品に付着又は混入している異物を除去する異物除去工程とを、上記加熱処理工程の前工程として実行するようにすることができる(請求項2)。この場合、廃棄アルミ製品の収集や、収集後の取扱い等の実情に即したリサイクル処理方法を特定し得ることになる。そして、解放工程により分離された廃棄アルミ製品はその状態のままで異物除去工程が行われるため、廃棄アルミ製品を先に破砕・裁断した上で異物除去する従来方法よりも異物除去を容易にかつ確実に行い得ることになり、最終のリサイクル製品となるアルミブリケットの高純度化に寄与し得ることになる。 In this invention, when a large number of waste aluminum products are used as press raw materials in a state of light compression molding into a rectangular shape, the press scrap is released from the light compression molding state and separated into individual waste aluminum products. A foreign matter removing step for removing foreign matter adhering to or mixed in the waste aluminum product from the waste aluminum product in an individually separated state as a pre-step of the heat treatment step. (Claim 2). In this case, it is possible to specify a recycling method in accordance with the actual situation such as collection of waste aluminum products and handling after collection. Since the waste aluminum product separated in the release process is subjected to the foreign matter removal process in that state, it is easier to remove the foreign matter than the conventional method of removing the foreign matter after first crushing and cutting the waste aluminum product. It can be performed reliably, and can contribute to the high purity of the aluminum briquette that will be the final recycled product.
又、ブリケット成型工程により成型されたアルミブリケットをリサイクル製品として再利用する用途に応じたサイズに切断する切断工程を、ブリケット成型工程の後工程として実行するようにすることができる(請求項3)。この場合、リサイクル製品が再利用される用途等に応じて最適なサイズ・重量に調整することが可能となって、取扱い性や再利用の確実性の向上が図られることになる。 In addition, the cutting step of cutting the aluminum briquette formed by the briquetting molding step into a size corresponding to the purpose of reuse as a recycled product can be executed as a subsequent step of the briquetting molding step. . In this case, it is possible to adjust the size and weight to the optimum according to the application for which the recycled product is reused, and the handling property and the certainty of reuse are improved.
さらに具体的には、廃棄アルミ製品として使用済みのアルミ缶を対象にし、加熱処理工程を400℃〜500℃の温度範囲で乾留し、破砕工程で幅15mm以下のアルミ細片に破砕・裁断し、ブリケット成型工程で2.2g/cm3以上の比重を有するアルミブリケットに圧縮固化するようにすることができる(請求項4)。この場合、使用済みのアルミ缶を出発原料としてリサイクル製品を製造するためのリサイクル処理方法として具体化させ得ることになる。すなわち、上記の温度範囲で加熱することにより酸化を確実に防止した状態で表面塗料等の熱分解による除去が図られ、幅15mm以下のアルミ細片に裁断することにより、そのアルミ細片を材料にして圧縮固化させたアルミブリケットを確実に2.2g/cm3以上の高比重に成型し得ることになる。 More specifically, for used aluminum cans as waste aluminum products, the heat treatment process is dry-distilled in the temperature range of 400 ° C to 500 ° C, and crushing and cutting into aluminum strips with a width of 15 mm or less in the crushing process. In the briquette molding step, it can be compressed and solidified into an aluminum briquette having a specific gravity of 2.2 g / cm 3 or more. In this case, it can be embodied as a recycling method for producing a recycled product using a used aluminum can as a starting material. That is, it is removed by thermal decomposition of the surface paint, etc. in a state in which oxidation is reliably prevented by heating in the above temperature range, and the aluminum strip is cut into an aluminum strip having a width of 15 mm or less to make the aluminum strip a material. Thus, the compressed and solidified aluminum briquette can be reliably molded to a high specific gravity of 2.2 g / cm 3 or more.
以上、説明したように、請求項1〜請求項4のいずれかのアルミ缶のリサイクル処理方法によれば、加熱処理工程により、廃棄アルミ製品を酸化させることなく表面処理された塗料やコーティング材、あるいは、表面に付着した水分や不純物を熱分解させることができ、これにより、廃棄アルミ製品から本来の素材であるアルミニウム合金以外の不純物を確実に除去することができる共に、焼き鈍すことができるようになる。次に、破砕工程において加熱処理後の廃棄アルミ製品を破砕・裁断することにより生成したアルミ細片をブリケット成形工程で圧縮固化して高比重・高純度のアルミブリケットを得ることができ、このアルミブリケットにより脱酸材等の製鋼用副原料又は新たなアルミ製品の原料等として再利用されるリサイクル製品を得ることができるようになる。特に加熱処理工程において、密閉可能な加熱炉と、循環ファンと、加熱ガス発生室とを用い、加熱炉での乾留により生成される熱分解ガスを加熱ガス発生室において燃焼させその燃焼排ガスを加熱炉に戻すようにしているため、加熱処理工程における還元雰囲気での加熱処理を確実に行うことができるようになる。 As described above, according to the method for recycling aluminum cans according to any one of claims 1 to 4, a paint or coating material that has been surface-treated without oxidizing waste aluminum products by a heat treatment step, Alternatively, moisture and impurities adhering to the surface can be thermally decomposed, so that impurities other than the aluminum alloy that is the original material can be surely removed from the discarded aluminum product and annealed. become. Next, the aluminum pieces produced by crushing and cutting the waste aluminum product after heat treatment in the crushing process can be compressed and solidified in the briquette forming process to obtain aluminum briquettes with high specific gravity and high purity. By using briquette, it becomes possible to obtain a recycled product that is reused as a secondary material for steelmaking such as a deoxidizing material or a raw material for a new aluminum product. In particular, in the heat treatment process, a heatable furnace that can be sealed, a circulation fan, and a heated gas generation chamber are used to heat the combustion exhaust gas by burning pyrolysis gas generated by dry distillation in the heating furnace in the heated gas generation chamber. Since it is made to return to a furnace, the heat processing in the reducing atmosphere in a heat processing process can be performed reliably.
請求項2によれば、前工程として解放工程及び異物除去工程の追加によって、廃棄アルミ製品の収集や、収集後の取扱い等の実情に即したリサイクル処理方法を特定することができる。特に、解放工程により分離された廃棄アルミ製品の状態のままで異物除去工程が行われるため、廃棄アルミ製品を先に破砕・裁断した上で異物除去する従来方法よりも異物除去を容易にかつ確実に行うことができ、これに伴い、最終のリサイクル製品となるアルミブリケットの高純度化を図ることができるようになる。 According to the second aspect, by adding the release step and the foreign matter removal step as the pre-process, it is possible to specify a recycling method that meets the actual situation such as collection of waste aluminum products and handling after the collection. In particular, since the foreign matter removal process is performed in the state of the waste aluminum product separated by the release process, foreign matter removal is easier and more reliable than the conventional method of removing foreign matter after first crushing and cutting the waste aluminum product. As a result, the aluminum briquette that will be the final recycled product can be highly purified.
又、請求項3によれば、後工程として切断工程を追加することにより、リサイクル製品が再利用される用途等に応じて最適なサイズ・重量に調整することができ、取扱い性や再利用の確実性の向上を図ることができるようになる。 In addition, according to claim 3, by adding a cutting step as a post-process, it is possible to adjust the size and weight to the optimum size according to the application for which the recycled product is reused. Certainty can be improved.
さらに、請求項4によれば、使用済みのアルミ缶を出発原料としてリサイクル製品を製造するためのリサイクル処理方法として具体化させることができる。すなわち、400℃〜500℃の温度範囲で加熱することにより酸化を確実に防止した状態で表面塗料等の除去を図ることができ、幅15mm以下のアルミ細片に裁断することにより、そのアルミ細片を材料にして圧縮固化させたアルミブリケットを確実に2.2g/cm3以上の高比重に成型することができるようになる。
Furthermore, according to the fourth aspect, the present invention can be embodied as a recycling method for manufacturing a recycled product using a used aluminum can as a starting material. That is, it is possible to remove the surface paint and the like in a state in which oxidation is reliably prevented by heating in a temperature range of 400 ° C. to 500 ° C. An aluminum briquette made by compressing and solidifying a piece as a material can be reliably molded to a high specific gravity of 2.2 g / cm 3 or more.
以下、本発明の実施形態を図面に基づいて説明する。 Hereinafter, embodiments of the present invention will be described with reference to the drawings.
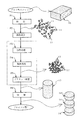
図1は、本発明の実施形態に係る廃棄アルミ製品のリサイクル処理方法の工程図を示す。本発明は、還元雰囲気において乾留させ得る乾留還元型の加熱炉を用いた加熱処理工程P3と、加熱処理後にシュレッダーを用いて破砕・裁断してアルミ細片にする破砕処理工程P4と、破砕処理後のアルミ細片を材料にしてブリケットマシンによりアルミブリケットに成型するブリケット成型工程P5とを組み合わせた点に特徴がある。すなわち、加熱処理工程P3により、廃棄アルミ製品を酸化させることなく表面処理された塗料やコーティング材、あるいは、表面に付着した水分や不純物を熱分解させる。この加熱処理工程P3により、廃棄アルミ製品から本来の素材であるアルミニウム合金以外の不純物(上記の塗料等を含む)を除去すると共に、焼き鈍す。次に、破砕工程P4において、焼き鈍された加熱処理後の廃棄アルミ製品をシュレッダーで破砕・裁断してアルミ細片(例えば幅15mm程度以下)にして、このアルミ細片をブリケット成形工程P5でブリケットマシンにより所定圧縮力で所定サイズに成型・固化することにより、所定の高比重・高純度のアルミブリケットを得る。 FIG. 1 is a process diagram of a recycling method for waste aluminum products according to an embodiment of the present invention. The present invention includes a heat treatment process P3 using a dry distillation reduction-type heating furnace that can be carbonized in a reducing atmosphere, a crushing process process P4 that is shredded and cut into pieces of aluminum using a shredder after the heat treatment, and a crushing process. It is characterized in that it is combined with a briquette molding step P5 in which a later aluminum strip is used as a material and molded into an aluminum briquette by a briquette machine. That is, in the heat treatment step P3, the paint or coating material that has been surface-treated without oxidizing the waste aluminum product, or moisture and impurities attached to the surface are thermally decomposed. By this heat treatment process P3, impurities (including the above-mentioned paint and the like) other than the original aluminum alloy are removed and annealed from the discarded aluminum product. Next, in the crushing step P4, the annealed waste aluminum product after heat treatment is crushed and cut with a shredder to form aluminum strips (for example, about 15 mm or less in width), and the aluminum strips in the briquette forming step P5. A predetermined high specific gravity and high purity aluminum briquette is obtained by molding and solidifying into a predetermined size with a predetermined compression force by a briquette machine.
次に、廃棄アルミ製品として使用済みアルミ缶を対象にした具体的な一例について説明する。ここで、アルミ缶とは、アルミニウム合金(以下、単に「アルミニウム」という)により製造された飲料缶のことであり、一般に、胴部分がA3000系のアルミニウム合金により形成され、蓋部分がA5000系のアルミニウム合金により形成されたものである。 Next, a specific example for a used aluminum can as a waste aluminum product will be described. Here, the aluminum can is a beverage can made of an aluminum alloy (hereinafter simply referred to as “aluminum”). Generally, the body portion is made of an A3000 series aluminum alloy and the lid portion is made of an A5000 series. It is formed of an aluminum alloy.
一般に、使用済みのアルミ缶は廃棄物回収業者により分別収集されるか、スチール缶等と混合状態で収集された後にスチール缶等と選別されるかした後、それらのアルミ缶をリサイクル処理業者に供給するために、いわゆるアルミ缶スクラップと言われる矩形状の塊とされる。このアルミ缶スクラップ10は所定量ずつまとめて軽プレスされて個々のアルミ缶が軽く潰された状態に圧縮成形されたものであり、主として運搬及び取扱いの便宜のために形成されるものである。このようなアルミ缶スクラップ10の供給を受けたリサイクル処理業者において、以下に説明するような各処理工程P1〜P6が実施されて製鋼用副原料(例えば脱酸材)等として再利用されるリサイクル製品14,14,…となる。
Generally, used aluminum cans are collected separately by a waste collection company or collected in a mixed state with steel cans and then sorted into steel cans. In order to supply, it is made into a rectangular lump called so-called aluminum can scrap. The aluminum can scrap 10 is lightly pressed together by a predetermined amount and compressed and molded into a state where individual aluminum cans are lightly crushed, and is formed mainly for convenience of transportation and handling. Recycling companies that have supplied such aluminum can scrap 10 are recycled as steelmaking auxiliary materials (for example, deoxidizing materials) after the processing steps P1 to P6 described below are performed.
製鋼用副原料としてのリサイクル製品14を製造するための処理方法としては、出発原料がアルミ缶スクラップ10であることに起因して必要となる処理や比較的容易に選別し得る異物を除去するために処理等の前処理工程と、リサイクル製品として備えるべき品質を具備させるために必要な処理である本処理工程と、リサイクル製品の使用先に応じたサイズ・重量等の仕様に調整するために必要となる後処理工程とに分かれる。前処理工程は解放工程P1及び異物除去工程P2を備えたものであり、本処理工程は加熱処理工程P3、破砕処理工程P4及びブリケット成型工程P5を備えたものであり、後処理工程は切断工程P6を備えたものである。
As a processing method for manufacturing a
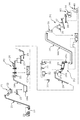
以下、図1に加えて図2をも参照しつつ、各工程を詳細に説明する。解放工程P1は、アルミ缶スクラップ10に対し衝撃力や振動力を加えてアルミ缶スクラップ10から個々の1枚毎のアルミ缶11,11,…の状態にバラバラに分離・解放して分解するための処理であり、いわゆる解放機といわれる装置を用いてアルミ缶各スクラップ10からアルミ缶11,11,…を破砕することなく1枚ずつ剥がすものである。この解放工程P1では、アルミ缶スクラップ10をストックヤードから例えばショベルローダ等で搬送して投入コンベア21に所定タイミング毎に載せ、この投入コンベア21により解放機としての例えば衝撃式一軸破砕機22に投入する。この衝撃式一軸破砕機22内で回転させながら衝撃力を加えて結合を解いて引き剥がし、さらに振動フィーダ23にて解放後の衝撃を吸収させながら1缶ずつにバラバラに分散させ、この1缶ずつにバラバラに分散された状態のアルミ缶11,11,…を次工程の異物除去工程P2に送る。振動フィーダ23としては、例えば下部バイブレータコイルスプリング支持方式のものを用いればよい。
Hereinafter, each process will be described in detail with reference to FIG. 2 in addition to FIG. In the release process P1, an impact force or a vibration force is applied to the aluminum can scrap 10 to separate and release the aluminum can scrap 10 into
解放工程P1から異物除去工程P2への搬送は、例えば、テールにホッパー24aを装備したエプロンコンベア24を用いればよい。すなわち、上記振動フィーダ23から1缶ずつバラバラの状態のアルミ缶11,11,…をホッパー24a内に投入して貯め、ホッパー24aの底部からエプロンコンベア24に対し定量ずつ落とし込んで次工程の手選別コンベア25まで定量搬送させる。ここで、エプロンコンベアとは、急傾斜(例えば45度の傾斜角)にて大量搬送し得るチェーンコンベアのことであり、エプロンといわれる板をコンベアチェーンに取り付け、コンベアチェーンを進行させることにより搬送物を上方位置まで搬送するものである。
For example, an
異物除去工程P2は、手選別による異物・危険物等の選別・除去と、磁選(磁力選別)によるスチール異物の選別・除去とをそれぞれ行うものである。手選別は上記のエプロンコンベア24により定量供給されるアルミ缶11,11,…を手選別コンベア25に流しながら作業者の視認に基づき行い、磁選は磁選機(例えば永久磁石式吊り下げベルト型磁選機)26によりスチール異物(例えば釘,ネジ等)の選別と自動排出とを行うようにすればよい。手選別の対象は、アルミ缶11,11,…に混在している異物(例えば飲料用空缶以外の食缶、菓子缶、その他)や危険物(スプレー缶等)であり、手選別した異物や危険物をコンテナC1に回収して処分する。
The foreign matter removing process P2 performs sorting / removal of foreign matter / dangerous materials by manual sorting, and sorting / removal of steel foreign matter by magnetic sorting (magnetic sorting). The hand sorting is performed based on the operator's visual recognition while flowing the
異物除去工程P2を経たアルミ缶11,11,…は、例えば一時貯留機能及び定量払い出し機能を有する貯留槽付きのプールコンベア27と、定量・連続供給可能なエプロンコンベア28とからなる定量供給手段によって、次工程の加熱処理P3の加熱炉29に対し加熱炉29での均一加熱を実現させるために所定流量の定量供給でかつ連続供給される。
The
加熱処理P3では、アルミ缶11,11,…に対し非酸素的雰囲気の還元条件下で焼成状態となる所定温度の高温不活性ガスに晒すことによりアルミ缶11の表面塗料やコーティングを熱分解させ、これにより、アルミ缶11の酸化を防止しつつアルミ缶11から本来のアルミニウム合金以外の不純物を除去すると同時に、アルミ缶11を焼成する。 In the heat treatment P3, the surface paint or coating of the aluminum can 11 is thermally decomposed by exposing the aluminum can 11, 11,... To a high temperature inert gas at a predetermined temperature that is fired under reducing conditions in a non-oxygen atmosphere. Thus, while preventing oxidation of the aluminum can 11, impurities other than the original aluminum alloy are removed from the aluminum can 11, and at the same time, the aluminum can 11 is fired.
このような加熱処理P3を実現するための設備として、本実施形態では、無酸素又は酸素が殆ど存在しないような非酸素的雰囲気に維持されて還元条件下でアルミ缶11,11,…を乾留させ得るように構成された還元乾留型の加熱炉(ロータリキルン)29を用いる。この加熱炉29は、入口側にエプロンコンベア28により定量供給されるアルミ缶11,11,…を貯めるホッパー29aと、二重のダンパ29bとが付設される一方、出口側にも二重のダンパ29cが付設され、それぞれの二重のダンパ29b,29cの交互開閉によって内部を密閉状態に維持したままで加熱対象のアルミ缶11,11,…の供給(投入)が可能となっている。又、上記加熱炉29には、サイクロン集塵機30と、循環ファン31と、完全燃焼炉により構成された加熱ガス発生室32とが付設され、加熱炉29での乾留により生じた熱分解ガス(可燃ガス)を導出して完全燃焼させる一方、その燃焼排ガスを加熱炉29に環流させてアルミ缶11,11,…を加熱するようにしている。
As an equipment for realizing such heat treatment P3, in the present embodiment, the
そして、循環ファン31の作動により、加熱炉29内で生じるアルミニウム粉塵を含む熱分解ガスを加熱炉29から導出してサイクロン集塵機30に送り、サイクロン集塵機30においてアルミニウム粉塵を熱分解ガスから分離回収し、アルミニウム粉塵を除去した残りの熱分解ガスが加熱ガス発生室32に送られる。加熱ガス発生室32では外部の燃料供給源(例えばLPガスボンベ)33からの燃料ガス(例えばLPガス)の供給を受けて、この燃料ガスと上記熱分解ガスとを完全燃焼させ、完全燃焼後の高温度の燃焼ガス(燃焼排ガス)を焼成条件となる温度でかつアルミ缶11の酸化を防止し得る所定温度に調整した後に加熱炉29内に環流させる。これにより、加熱炉29内を、アルミ缶11の酸化防止を確実に図ることができ、かつアルミニウム合金の融点よりも低い焼成温度条件で しかもアルミ缶11の表面塗料やコーティング等の不純物を熱分解させ得る温度条件にするようにする。このような温度条件としては、400℃〜500℃の温度範囲、好ましくは400℃〜450℃の温度範囲でアルミ缶11,11,…を加熱し得るものであり、とりわけアルミ缶11,11,…に対する加熱温度が実質的に410℃になるようにすることが好ましい。なお、サイクロン集塵機30で分離回収されたアルミニウム粉塵は、アルミニウムの焼成粉としてリサイクル製品の一種類となし得る。又、加熱ガス発生室32での余剰ガスは冷却処理後にバグフィルタを通して大気に放出される。
Then, by the operation of the
次に、加熱処理により焼成された状態のアルミ缶(以後「アルミ焼成缶」という)を次工程の破砕処理工程P4により破砕・裁断してアルミ細片12とする。この際、加熱炉29から出口側のダンパ29cを経て出されたアルミ焼成缶は例えば急傾斜エプロンコンベアにより構成された出口コンベア34に導出され、出口コンベア34により搬送される間に空冷された後、排出切り替えが可能な切替ダンパシュート35を経てシュレッダー36に投入される。これにより、搬送ラインに例えば所定量以上のアルミ焼成缶が流出した場合などの異常事態が発生したときに、切替ダンパシュート35を異常排出側に切り替えして、その増分のアルミ焼成缶をコンテナC2に排出し得るようにし、以後の各工程P4,P5,P6の連続運転を維持し得るようになっている。コンテナC2に貯留されたアルミ焼成缶は出口コンベア34の入口側に再び戻すことができる。
Next, the aluminum can that has been baked by the heat treatment (hereinafter referred to as “aluminum baked can”) is crushed and cut into the aluminum strips 12 in the subsequent crushing process P4. At this time, the aluminum calcined can taken out from the
破砕処理工程P4で用いるシュレッダー36としては例えば一軸式粉砕機を用いればよい。一軸式粉砕機は、超硬回転刃と固定刃との間にホッパーから投入したアルミ焼成缶を噛み込ませて破砕・裁断し、下側のスクリーンの開口サイズ以下のものが加工後のアルミ細片12として排出され、それよりも大きいものは掻き上げられて上記の破砕・裁断が繰り返されるようになっている。この破砕処理工程P4により生成されるアルミ細片12としては、破砕幅(裁断幅)をほぼ15mm以下とすることが、次工程のブリケット成型工程P5によるブリケット13の要求品質である高比重化にとって好ましい。とりわけ、破砕幅を実質的に10mm以下にして嵩比重0.7t/m3程度にすることが好ましい。又、破砕効率上、回転刃としてVの字型に配置したものが好ましい。
As the
ブリケット成型工程P5では、アルミ細片12,12,…を圧縮固化してリサイクル製品として要求される形状及び高比重を有するブリケット13を成型する。形状としては円形又は楕円形との断面を有する円柱状、あるいは、三角形又は四角形等の断面を有する角柱状に成型すればよく、サイズとしては形状が円柱状の場合には最大で直径が100mm程度、好ましくは直径を60〜80mm程度にすればよく、又、圧縮の程度としては比重が例えば実質的に2.2g/cm3以上のものにすればよい。このようなブリケット13を成型するためには、所定量のアルミ細片12,12,…を型内に充填し、これを例えば294MPa(3t/cm2)程度の圧縮面圧でプレス加工すればよい。以上により、高純度でかつ内部まで均一な比重を有し、しかも要求される高比重(2.2g/cm3程度以上)を有するブリケット13を成型することができる。
In the briquette molding process P5, the aluminum strips 12, 12,... Are compressed and solidified to mold the
このブリケット成型工程P5はブリケット成型機39を用いて行うようにし、このブリケット成型機39に対し切断機40を附属させて切断工程P6を行うようにしている。これに対しアルミ細片12,12,…を供給するために、シュレッダー36から排出されたアルミ細片12,12,…をベルトコンベア37に落とし、続いてベルトコンベア38によりブリケット成型機39に対し個別に供給させ得るようにしている。又、後述の切断工程P6で生じた切断屑をブリケット成型工程P5に戻してアルミ細片12と共に圧縮固化させることにより、歩留まりの向上を図り高比重化に寄与させるようにしている。
The briquette molding process P5 is performed using a
切断工程P6では、ブリケット13がそのままのサイズ・重量ではリサイクル製品としては大きすぎたり重すぎたりする場合に、そのブリケット13をリサイクル製品の用途に応じた重量及びサイズになるように切断して最終のリサイクル製品とするものである。この切断工程P6を実行するための切断機40a,40bとしては、切断効率を考慮して例えば超硬丸鋸を備えたアルミ用丸鋸切断機を用いるようにすればよい。製鋼用副原料(脱酸材)としての用途では、ブリケット13が例えば直径80mm程度のものであれば、長さ18mm程度に切断すれば重量200g程度となった平べったい円柱状の切断ピース14,14,…にすることができる。このような扁平な切断ピース14、つまり両端面が平坦面を有し直径に比して両端面間の高さ(長さ)が極めて短いような扁平形状の切断ピース14とすることにより、リサイクル製品の使用時の取り扱い性、特にコンベア搬送時の安定性を十分に確保することができるようになり、転げ落ちる等の不都合発生等を確実に回避することができるようになる。
In the cutting process P6, when the
以上の本実施形態によるリサイクル処理方法の場合、使用済みのアルミ缶を原料にして、従来方法における造粒工程を省略してペレット化(造粒化)することなく、製鋼用副原料(脱酸材)として再利用し得る高比重(例えば2.2g/cm3)・高純度(例えばアルミニウム合金成分が96重量%以上)のリサイクル製品14を製造することができるようになる。このため、従来方法では必要としていた造粒機の設置自体を省略することができ、これに伴い、造粒機の損耗に起因するメンテナンス頻度の増大や歩留まりの悪化を阻止してそれらに要するコストの削減化及び駆動用の電力エネルギーの削減化を共に実現させることができる。又、リサイクル製品としての切断ピース14は、搬送コンベアに載せられても姿勢が安定する形状であるため、最終溶解炉まで安定供給することができる上に、所要の重量を備えているため最終溶解炉に対し投入されれば炉内下部まで確実に到達させることができるようになり、製鋼品質の向上にも寄与させることができる。さらに、加熱処理前に裁断して細片化する従来方法と異なり、加熱処理前にはアルミ缶スクラップ10から1枚毎のアルミ缶11に分離させた状態で異物除去工程P2を行い、加熱処理工程P3の後に破砕処理工程P4を行うようにしているため、特に、磁選し得るスチール異物以外の異物の除去をより一層容易かつ確実に行うことができる。これにより、異物混入のままアルミペレットに成形される場合が発生し易い従来方法と比べ、本実施形態では最終のリサイクル製品における高純度化を図ることができるようになる。
In the case of the recycling method according to the present embodiment as described above, a secondary material for steelmaking (deoxidation) is obtained by using a used aluminum can as a raw material, omitting the granulation step in the conventional method and pelletizing (granulating). The
又、特に、加熱前の段階においてアルミ缶を破砕することなく手選別や磁選により異物除去を行っている点、及び、加熱処理工程P3において表面塗料等を還元雰囲気下において熱分解(乾留)により除去させている点により、最終のリサイクル製品13,14の高純度化をより一層図ることができる。さらに、加熱処理工程P3により焼き鈍されている上に破砕処理工程P4で細片化されたアルミ細片13を材料にしてブリケット成型工程P5を行っているため、最終のリサイクル製品13,14の高比重化もより一層図ることができることになる。
In particular, the foreign matter is removed by manual selection or magnetic separation without crushing the aluminum can in the stage before heating, and the surface coating or the like is subjected to thermal decomposition (dry distillation) in a reducing atmosphere in the heat treatment step P3. Due to the removal, it is possible to further increase the purity of the final
なお、上記の出口コンベア34のカバー34a内、シュレッダー36内、ブリケット成型機39内、及び、切断機40内の各所から図示省略の集塵ダクトを通してアルミニウム粉塵を含むダストを図示省略のサイクロン集塵機に集塵し、このサイクロン集塵機においてアルミニウム粉塵を回収し、アルミニウム粉塵除去後に残る主としてカーボンを含む細粉を図示省略のバグフィルタにより回収するようにしている。これらのアルミニウム粉塵やカーボン細粉は、別途再利用することができる。
It should be noted that dust containing aluminum dust passes through a dust collection duct (not shown) from various places in the
<他の実施形態>
なお、本発明は上記実施形態に限定されるものではなく、その他種々の実施形態を包含するものである。すなわち、上記実施形態では、主として使用済みの飲料用容器であるアルミ缶をリサイクル製品の原料として説明したが、これに限らず、例えば他のアルミニウム製容器やアルミニウムサッシ等のアルミニウム合金を素材にして製造され、その後に廃棄されることになったアルミニウム製品をリサイクル製品の原料にして本実施形態のリサイクル処理方法を適用するようにしてもよい。これらの場合、アルミ缶スクラップと同様に、廃棄アルミ製品は廃棄物収集業者において軽プレスされてアルミスクラップの形態でリサイクル処理業者に供給され、リサイクル処理業者ではこの形態からリサイクル処理を開始することになるため、以上の本実施形態を適用し得る。
<Other embodiments>
In addition, this invention is not limited to the said embodiment, Various other embodiments are included. That is, in the embodiment described above, aluminum cans, which are mainly used beverage containers, have been described as raw materials for recycled products. However, the present invention is not limited thereto, and other aluminum containers and aluminum alloys such as aluminum sashes are used as materials. You may make it apply the recycling processing method of this embodiment by making the aluminum product manufactured and discarded after that into the raw material of a recycled product. In these cases, as with aluminum can scrap, waste aluminum products are lightly pressed at a waste collector and supplied to a recycling processor in the form of aluminum scrap, and the recycling processor starts recycling processing from this form. Therefore, the above embodiment can be applied.
又、上記実施形態では、アルミ缶を対象にした場合であって、これらをアルミ缶スクラップしたものを出発原料にした場合について説明したが、これに限らず、アルミ缶を対象にする場合であっても、アルミ缶スクラップの形態にすることなく、収集されたアルミ缶を対象にして異物除去工程P2から開始するようにしても、もちろんよい。 In the above embodiment, the case where aluminum cans are targeted and the scraps of these aluminum cans are used as starting materials has been described. However, it is of course possible to start the foreign matter removing step P2 for the collected aluminum cans without using the form of aluminum can scrap.
P1 解放工程
P2 異物除去工程
P3 加熱処理工程
P4 破砕処理工程
P5 ブリケット成型工程
P6 切断工程
29 加熱炉
31 循環ファン
32 加熱ガス発生室
P1 Release process P2 Foreign matter removal process P3 Heat treatment process P4 Crushing process P5 Briquette molding process
Claims (4)
加熱処理工程後に破砕・裁断してアルミ細片にする破砕処理工程と、
破砕処理工程後のアルミ細片を圧縮固化させてアルミブリケットに成型するブリケット成型工程と
を備え、
上記加熱処理工程において、密閉可能な加熱炉と、循環ファンと、加熱ガス発生室とを用い、循環ファンの作動により上記加熱炉での加熱により生成された熱分解ガスを加熱ガス発生室に循環供給し、この加熱ガス発生室で熱分解ガスを燃焼させることにより発生する燃焼排ガスを上記加熱炉に対し還元雰囲気で乾留させる加熱源として供給するようにする、ことを特徴とする廃棄アルミ製品のリサイクル処理方法。 A heat treatment step in which the waste aluminum product is subjected to dry distillation in a predetermined temperature range which is a firing temperature condition and a temperature condition capable of preventing oxidation in a heating furnace in a reducing atmosphere;
Crushing process after crushing and cutting after heat treatment process into aluminum pieces,
A briquette molding process that compresses and solidifies the aluminum pieces after the crushing process and molds them into aluminum briquettes;
In the heat treatment step, a heatable furnace, a circulation fan, and a heating gas generation chamber are used, and the pyrolysis gas generated by heating in the heating furnace is circulated to the heating gas generation chamber by the operation of the circulation fan. The waste aluminum product is characterized in that it is supplied as a heat source for dry distillation of the combustion exhaust gas generated by burning pyrolysis gas in the heating gas generation chamber in a reducing atmosphere to the heating furnace. Recycling method.
多数の廃棄アルミ製品が矩形形状に軽圧縮成形された状態のプレススクラップを出発原料にして、このプレススクラップを軽圧縮成形状態から解放して個々の廃棄アルミ製品に分離する解放工程と、個々に分離された状態の廃棄アルミ製品からこの廃棄アルミ製品に付着又は混入している異物を除去する異物除去工程とを、上記加熱処理工程の前工程として実行するようにする、廃棄アルミ製品のリサイクル処理方法。 A method for recycling waste aluminum according to claim 1,
A release process in which a large number of waste aluminum products are lightly compression-molded into a rectangular shape as a starting material, and the press scrap is released from the light compression-molded state and separated into individual waste aluminum products. A waste aluminum product recycling process in which a foreign matter removing step for removing foreign matter adhering to or mixed in the waste aluminum product from the separated waste aluminum product is executed as a pre-process of the heat treatment step. Method.
ブリケット成型工程により成型されたアルミブリケットをリサイクル製品として再利用する用途に応じたサイズに切断する切断工程を、ブリケット成型工程の後工程として実行するようにする、廃棄アルミ製品のリサイクル処理方法。 A method for recycling aluminum waste products according to claim 1 or claim 2,
A recycling method for waste aluminum products, wherein a cutting process for cutting aluminum briquettes formed by the briquetting molding process into a size corresponding to the purpose of reuse as a recycled product is performed as a subsequent process of the briquetting molding process.
廃棄アルミ製品として使用済みのアルミ缶を対象にし、加熱処理工程を400℃〜500℃の温度範囲で乾留し、破砕工程で幅15mm以下のアルミ細片に破砕・裁断し、ブリケット成型工程で2.2g/cm3以上の比重を有するアルミブリケットに圧縮固化するようにする、廃棄アルミ製品のリサイクル処理方法。 A recycling method for waste aluminum products according to any one of claims 1 to 3,
Targeting used aluminum cans as waste aluminum products, the heat treatment process is dry-distilled in the temperature range of 400 ° C to 500 ° C, crushing and cutting into aluminum strips with a width of 15 mm or less in the crushing process, and 2 in the briquette molding process A method for recycling waste aluminum products that is compressed and solidified into aluminum briquettes having a specific gravity of 2 g / cm 3 or more.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008318969A JP5404019B2 (en) | 2008-12-15 | 2008-12-15 | Recycling method for waste aluminum products |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008318969A JP5404019B2 (en) | 2008-12-15 | 2008-12-15 | Recycling method for waste aluminum products |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2010138478A JP2010138478A (en) | 2010-06-24 |
| JP5404019B2 true JP5404019B2 (en) | 2014-01-29 |
Family
ID=42348846
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2008318969A Expired - Fee Related JP5404019B2 (en) | 2008-12-15 | 2008-12-15 | Recycling method for waste aluminum products |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP5404019B2 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110153343A (en) * | 2019-06-05 | 2019-08-23 | 浙江蔚华汽车科技有限公司 | A kind of novel aluminum alloy formed solid method |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ES2398305B1 (en) * | 2011-03-08 | 2014-01-24 | Recuperación Medioambientales Industriales, S.L. | ECO-INSTALLATION OF METAL CHATARRA TREATMENT OF DIFFERENT NATURE. |
| CN103464443A (en) * | 2013-09-09 | 2013-12-25 | 昆山奥德鲁自动化技术有限公司 | Recovery method of metal waste during machining process |
| KR101909193B1 (en) * | 2018-04-26 | 2018-12-10 | 주식회사 피케이지 | An Apparatus for Manufacturing a Deoxidizer and a Method for Producing the Same |
| CN108588332B (en) * | 2018-06-28 | 2020-08-04 | 韩国Pkg株式会社 | Deoxidizer production device and process for producing deoxidizer by using same |
| JP2020148414A (en) * | 2019-03-14 | 2020-09-17 | 三菱アルミニウム株式会社 | How to measure the temperature of the heating furnace and the heated body |
| CN114904887B (en) * | 2022-05-09 | 2023-03-21 | 安徽铜鼎轻金属新材料科技有限公司 | Aluminum alloy slag-aluminum separation stirring equipment |
| KR102828700B1 (en) * | 2022-08-26 | 2025-07-03 | 에스아이플로텍(주) | Apparatus for recycling aluminum chip |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6137934A (en) * | 1984-07-30 | 1986-02-22 | Mitsubishi Metal Corp | Regenerating method of al from waste al can |
| JPH01188637A (en) * | 1988-01-21 | 1989-07-27 | Shintouyou Kinzoku Kogyo Kk | Treatment of aluminum can scrap |
| JP2742670B2 (en) * | 1995-05-17 | 1998-04-22 | 日本磁力選鉱株式会社 | How to treat used steel cans |
| JPH1060547A (en) * | 1996-08-23 | 1998-03-03 | Aikoo Kk | Treatment of aluminum scrap into melting raw material for reverberatory furnace |
| JPH11309441A (en) * | 1998-02-27 | 1999-11-09 | Myuuzero Suishin Kiko Kk | High-grade steel and aluminum recovery system from steel cans |
| JP2002001292A (en) * | 2000-06-22 | 2002-01-08 | Masataka Hanashima | Resource recovery method from beverage cans |
| JP2003306722A (en) * | 2002-04-18 | 2003-10-31 | Akimichi Hatsuta | Method and apparatus for recovering metal material from metal waste adhering and mixing with organic matter |
| JP4758602B2 (en) * | 2003-09-04 | 2011-08-31 | 株式会社アールニッセイ | Briquette production equipment |
-
2008
- 2008-12-15 JP JP2008318969A patent/JP5404019B2/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110153343A (en) * | 2019-06-05 | 2019-08-23 | 浙江蔚华汽车科技有限公司 | A kind of novel aluminum alloy formed solid method |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2010138478A (en) | 2010-06-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP2010138478A (en) | Method for recycling waste aluminum product | |
| JP6384846B1 (en) | Separation of metals from shredder dust, conversion of organic combustible residues into fuel, effective utilization of inorganic residues, and treatment equipment | |
| CN1045315C (en) | Method and apparatus for recycling empty aluminum cans | |
| KR20230110485A (en) | Lithium ion battery recycling method, apparatus and system | |
| JP2008232522A (en) | Paper shredder dust disposal method and its system | |
| CN102776048A (en) | Preparation process for granular fuels | |
| JP7172936B2 (en) | Garbage sorting method and device | |
| JP2002067029A (en) | Method for recycling used plastics and molded articles for recycling | |
| JP3745619B2 (en) | Molding method of waste plastic granulation for chemical raw materials | |
| EP1428642B1 (en) | Method of manufacturing waste granulated plastics, and method for thermal decomposition of the plastics | |
| KR101550491B1 (en) | Crushing and sorting system for regenerating refuse and scrap iron | |
| JP2019019346A (en) | Method for recovering precious metals from incineration ash | |
| JPH07300355A (en) | Production of cement | |
| JP4522336B2 (en) | Recycling method of shredder dust and raw material for steelmaking | |
| JP3490904B2 (en) | Processing method and processing equipment for powder dust containing heavy metals | |
| JP3704284B2 (en) | Method for producing coke oven raw materials from general plastic waste | |
| JP2001116226A (en) | How to recycle shredder dust | |
| KR101859632B1 (en) | Recycling processing apparatus of waste aluminum using method for carbonizing and removing impurities | |
| CN108588332B (en) | Deoxidizer production device and process for producing deoxidizer by using same | |
| JP4031609B2 (en) | Waste plastic recycling method | |
| US20180340240A1 (en) | System and method for briquetting cyclone dust from decoating systems | |
| JP2742670B2 (en) | How to treat used steel cans | |
| JP4910349B2 (en) | Biomass fuel production system | |
| KR101909193B1 (en) | An Apparatus for Manufacturing a Deoxidizer and a Method for Producing the Same | |
| JP2001113231A (en) | How to sort shredder dust |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20100824 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20130228 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20130326 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20130527 |
|
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20130910 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20131029 |
|
| LAPS | Cancellation because of no payment of annual fees |