JP2024162705A - Large capacity polymer lithium ion battery packaging machine - Google Patents
Large capacity polymer lithium ion battery packaging machine Download PDFInfo
- Publication number
- JP2024162705A JP2024162705A JP2023078515A JP2023078515A JP2024162705A JP 2024162705 A JP2024162705 A JP 2024162705A JP 2023078515 A JP2023078515 A JP 2023078515A JP 2023078515 A JP2023078515 A JP 2023078515A JP 2024162705 A JP2024162705 A JP 2024162705A
- Authority
- JP
- Japan
- Prior art keywords
- packaging
- ion battery
- polymer lithium
- packaging mechanism
- cell
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/50—Manufacturing or production processes characterised by the final manufactured product
Landscapes
- Package Closures (AREA)
- Casings For Electric Apparatus (AREA)
- Sealing Battery Cases Or Jackets (AREA)
- Secondary Cells (AREA)
Abstract
Description
本発明は、電池加工技術分野に関し、具体的には、大容量重合物リチウムイオン電池の包装機に関する。 The present invention relates to the field of battery processing technology, and more specifically to a packaging machine for large-capacity polymer lithium-ion batteries.
リチウム電池の生産プロセスにおいて、セルの製作が完了した後に、パッケージング工程を行う必要がある。パッケージング工程は、熱プレスの方式で、セルの周囲を覆うアルミプラスチックフィルムの周辺を溶接して密閉空間を形成し、その空間内にセルを包み込む。 In the lithium battery production process, after the cell production is completed, the packaging process must be carried out. The packaging process uses a hot press method to weld the periphery of the aluminum plastic film that surrounds the cell to form an airtight space, and then encase the cell within that space.
大容量重合物リチウムイオン電池は、体積が比較的大きく、セルのトップシール及びボトムシールの長さが長く、セル本体にエアバッグを加えてパッケージングの長さが一般的には1200mmになるため、長さが1200mmを超える成形ブロックを製作する必要がある。これにより、パッケージングプロセスが困難になっている。従って、現在、大容量重合物リチウムイオン電池のパッケージング(包装)は、一般的に手作業で行われ、効率が悪い。 Large-capacity polymer lithium-ion batteries have a relatively large volume, long cell top and bottom seals, and an airbag is added to the cell body, resulting in a packaging length of typically 1200 mm, making it necessary to fabricate a molded block with a length of more than 1200 mm. This makes the packaging process difficult. Therefore, currently, packaging of large-capacity polymer lithium-ion batteries is generally performed manually, which is inefficient.
本発明は、セルパッケージングプロセスの効率が低下する問題を改善するための大容量重合物リチウムイオン電池包装機を提供することを目的とする。 The present invention aims to provide a large-capacity polymer lithium-ion battery packaging machine that improves the problem of reduced efficiency in the cell packaging process.
本発明の実施例は、以下のように実施される。 An embodiment of the present invention is implemented as follows:
大容量重合物リチウムイオン電池包装機は、間隔をあけて設けられた少なくとも1対の上パッケージング機構及び間隔をあけて設けられた少なくとも1対の下パッケージング機構と、第1の昇降機構と、セルを固定するためのセル治具と、前記セル治具と伝動可能に接続され、前記セル治具を前記上パッケージング機構と前記下パッケージング機構との間に搬入するための搬送機構と、を含み、前記上パッケージング機構及び前記下パッケージング機構は、それぞれ、パッケージング材料を溶接するための成形ブロックを有する成形装置を備え、前記上パッケージング機構の成形ブロックと前記下パッケージング機構の成形ブロックとは、高さ方向において間隔を持って対向し、前記第1の昇降機構は、前記上パッケージング機構の成形ブロックと前記下パッケージング機構の成形ブロックとを当接させる、又は、離間させるために、前記上パッケージング機構を前記下パッケージング機構に対して接近させる、又は、離間させるように駆動する。 The large-capacity polymer lithium-ion battery packaging machine includes at least one pair of upper packaging mechanisms spaced apart and at least one pair of lower packaging mechanisms spaced apart, a first lifting mechanism, a cell jig for fixing a cell, and a transport mechanism drivably connected to the cell jig for transporting the cell jig between the upper packaging mechanism and the lower packaging mechanism, the upper packaging mechanism and the lower packaging mechanism each include a molding device having a molding block for welding packaging material, the molding block of the upper packaging mechanism and the molding block of the lower packaging mechanism face each other with a gap in the height direction, and the first lifting mechanism drives the upper packaging mechanism to approach or move away from the lower packaging mechanism in order to abut or move away the molding block of the upper packaging mechanism and the molding block of the lower packaging mechanism.
支持フレームを含み、前記第1の昇降機構と前記上パッケージング機構とは、それぞれ、前記支持フレームに設けられ、前記上パッケージング機構は、第1の昇降ガイドバーをさらに含み、前記第1の昇降ガイドバーの一端は、前記上パッケージング機構の第1の固定板に接続されるとともに、前記上パッケージング機構の昇降方向に沿って延在し、前記第1の昇降ガイドバーは、前記支持フレームの貫通孔を貫通する。 The device includes a support frame, and the first lifting mechanism and the upper packaging mechanism are each provided on the support frame, and the upper packaging mechanism further includes a first lifting guide bar, one end of which is connected to a first fixed plate of the upper packaging mechanism and extends along the lifting direction of the upper packaging mechanism, and the first lifting guide bar passes through a through hole in the support frame.
前記搬送機構は、スクリューと、ガイドレールと、前記スクリューの回動を駆動するための駆動部とを含み、前記セル治具は、前記スクリューとねじ接続され、かつ、前記ガイドレールとスライド可能に接続され、前記スクリューの延在方向は、前記ガイドレールの延在方向と一致する。 The transport mechanism includes a screw, a guide rail, and a drive unit for driving the rotation of the screw, the cell jig is screw-connected to the screw and slidably connected to the guide rail, and the extension direction of the screw coincides with the extension direction of the guide rail.
前記セル治具は、前記セルを載置するための載置板と、前記セルを押圧するための押圧機構とを含み、前記押圧機構は、前記載置板の上方に設けられている。 The cell jig includes a mounting plate for mounting the cell and a pressing mechanism for pressing the cell, the pressing mechanism being provided above the mounting plate.
前記押圧機構は、鉛直方向に伸縮可能な押圧シリンダを含む。 The pressing mechanism includes a pressing cylinder that can expand and contract vertically.
前記セル治具は、前記ガイドレールとスライド可能に接続され、かつ、前記スクリューとねじ接続される基板を含み、前記載置板は、前記載置板を昇降するための第2の昇降機構を介して前記基板の上面と伝動可能に接続される。 The cell jig includes a base plate that is slidably connected to the guide rail and is screw-connected to the screw, and the mounting plate is movably connected to the upper surface of the base plate via a second lifting mechanism for raising and lowering the mounting plate.
前記載置板の下面には、前記載置板に垂直な第2の昇降ガイドバーが設けられ、前記第2の昇降ガイドバーは、前記基板の貫通孔に挿入されて前記基板とスライド可能に接続される。 A second lift guide bar is provided on the underside of the mounting plate, perpendicular to the mounting plate, and the second lift guide bar is inserted into a through hole in the substrate and slidably connected to the substrate.
前記載置板には、前記下パッケージング機構の成形ブロックを通過させるための1対の逃げ溝が設けられている。 The mounting plate has a pair of clearance grooves to allow the molding blocks of the lower packaging mechanism to pass through.
前記載置板には、前記セルの極タブを挟持するための2つの位置決めブロックが設けられている。 The mounting plate is provided with two positioning blocks for clamping the pole tabs of the cells.
前記成形ブロックには、前記成形ブロックを加熱するための加熱装置が設けられている。 The molding block is provided with a heating device for heating the molding block.
本発明の実施例の有益な効果は、以下のとおりである。 The beneficial effects of the embodiment of the present invention are as follows:
本発明の実施例による大容量重合物リチウムイオン電池包装機は、間隔をあけて設けられた少なくとも1対の上パッケージング機構及び間隔をあけて設けられた少なくとも1対の下パッケージング機構と、第1の昇降機構と、セルを固定するためのセル治具と、セル治具と伝動可能に接続される搬送機構とを含む。上パッケージング機構と下パッケージング機構とは、それぞれ、パッケージング材料を溶接するための成形ブロックを有する成形装置を備え、上パッケージング機構の成形ブロックと下パッケージング機構の成形ブロックとは、高さ方向において間隔を持って対向する。第1の昇降機構は、上パッケージング機構の成形ブロックと下パッケージング機構の成形ブロックとを当接させる、又は、離間させるために、上パッケージング機構を下パッケージング機構に対して接近させる、又は、離間させるように駆動する。上パッケージング機構と下パッケージング機構の成形ブロックとが当接する時に、アルミプラスチックフィルムを溶接してパッケージング効果を実現することができる。搬送機構は、セル治具を上パッケージング機構と下パッケージング機構との間に搬入するために用いられる。本発明の大容量重合物リチウムイオン電池包装機は、セルの挟持、搬送、パッケージングの機能を実現しており、電池パッケージング効率を大幅に向上させることができる。 A large-capacity polymer lithium-ion battery packaging machine according to an embodiment of the present invention includes at least one pair of upper packaging mechanisms spaced apart from each other and at least one pair of lower packaging mechanisms spaced apart from each other, a first lifting mechanism, a cell jig for fixing a cell, and a conveying mechanism operably connected to the cell jig. The upper packaging mechanism and the lower packaging mechanism each include a molding device having a molding block for welding a packaging material, and the molding block of the upper packaging mechanism and the molding block of the lower packaging mechanism face each other with a gap in the height direction. The first lifting mechanism drives the upper packaging mechanism to approach or move away from the lower packaging mechanism in order to bring the molding block of the upper packaging mechanism into contact with or away from the molding block of the lower packaging mechanism. When the molding blocks of the upper packaging mechanism and the lower packaging mechanism come into contact with each other, an aluminum plastic film can be welded to achieve a packaging effect. The conveying mechanism is used to carry the cell jig between the upper packaging mechanism and the lower packaging mechanism. The large-capacity polymer lithium-ion battery packaging machine of the present invention realizes the functions of clamping, transporting, and packaging cells, and can significantly improve battery packaging efficiency.
本発明の実施例の技術案をより明瞭に説明するために、以下、実施例に使用される必要な図面を簡単に説明する。以下の図面は、本発明のいくつかの実施例を例示するにすぎないため、本発明の範囲に対する限定と見なされるべきではなく、当業者にとって、創造的な労力を払わずにこれらの図面に基づいて他の関連図面を得ることもできると理解すべきである。
本発明の実施例の目的、技術案及び利点をより明瞭にするために、以下、本発明の実施例における図面を参照しながら、本発明の実施例における技術案を明瞭、且つ、包括的に説明し、当然、記述された実施例は、本発明の一部の実施例であり、すべての実施例ではない。一般的には、ここで図面において説明して示される本発明の実施例の構成要素は、様々な異なる配置でレイアウトして設計されてもよい。 In order to make the objectives, technical solutions and advantages of the embodiments of the present invention clearer, the technical solutions of the embodiments of the present invention will be described clearly and comprehensively below with reference to the drawings of the embodiments of the present invention. Of course, the described embodiments are only some of the embodiments of the present invention, and not all of the embodiments. In general, the components of the embodiments of the present invention described and shown in the drawings herein may be laid out and designed in various different configurations.
そのため、以下の図面において提供される本発明の実施例の詳細な説明は、保護しようとする本発明の範囲を制限するものではなく、本発明の好ましい実施例を表すものに過ぎない。当業者が本発明における実施例に基づいて創造的な労力を払わずに得られたすべての他の実施例もすべて本発明の保護範囲に属する。 Therefore, the detailed description of the embodiments of the present invention provided in the following drawings does not limit the scope of the invention to be protected, but merely represents a preferred embodiment of the present invention. All other embodiments obtained by a person skilled in the art based on the embodiments of the present invention without any creative effort also fall within the scope of protection of the present invention.
類似の符号及びアルファベットは、以下の図面において類似の構成要素を示すため、ある構成要素が一つの図面において定義されると、その後の図面においてそれについてさらなる定義及び解釈が必要としないと注意すべきである。 It should be noted that like numerals and letters indicate like components in the following drawings, so that once a component is defined in one drawing, it does not require further definition and interpretation in subsequent drawings.
本発明の実施例の説明において、「上」、「下」、「鉛直」、「水平」、などの用語により示される方位又は位置関係は、図面に基づいて示される方位又は位置関係、又は、この発明製品の使用時に通常配置される方位又は位置関係であり、本発明を説明しやすく、かつ、説明を簡略化するためのものにすぎず、かかる装置又は要素が特定の方位を有し、特定の方位で構成して操作しなければならないことを明示する、又は、暗示するものではないため、本発明を制限するためのものと解釈できないと理解すべきである。なお、「第1」、「第2」、「第3」などの用語は、単に表現を区別するために使用され、相対的な重要性を明示する、又は、暗示すると理解されない。 In the description of the embodiments of the present invention, the orientations or positional relationships indicated by terms such as "upper", "lower", "vertical", and "horizontal" are the orientations or positional relationships shown in the drawings, or the orientations or positional relationships in which the product of the present invention is normally disposed when in use, and are merely intended to facilitate and simplify the description of the present invention. They do not expressly or imply that such devices or elements have a specific orientation, or must be configured and operated in a specific orientation, and therefore should not be construed as limiting the present invention. In addition, terms such as "first", "second", and "third" are used merely to distinguish between expressions, and are not understood to express or imply relative importance.
本発明の実施例の説明において、さらに、説明すべきことは、特に明確に規定や限定されない限り、「設け」、「取付け」、「繋がり」、「接続」という用語は、広義に理解されるべきであり、例えば固定的な接続、取り外し可能な接続、又は一体的な接続であってもよく、機械的な接続又は電気的な接続であってもよく、直接的な繋がりであってもよく、中間媒体に介する間接的な繋がりであってもよく、2つの要素内部の連通であってもよい。当業者にとって、具体的な状況に応じて上記用語の本発明の実施例における具体的な意味を理解することができる。 In the description of the embodiments of the present invention, it should be further explained that unless otherwise clearly specified or limited, the terms "provided," "attached," "connected," and "connected" should be understood in a broad sense, and may be, for example, a fixed connection, a removable connection, or an integral connection, a mechanical connection or an electrical connection, a direct connection, an indirect connection via an intermediate medium, or internal communication between two elements. Those skilled in the art can understand the specific meaning of the above terms in the embodiments of the present invention according to the specific circumstances.
<実施例>
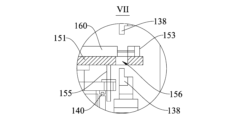
図4は、本発明の実施例による大容量重合物リチウムイオン電池包装機10の第1の視野角の模式図であり、図5は、本発明の実施例による大容量重合物リチウムイオン電池包装機10の第2の視野角の模式図であり、図6は、本発明の実施例による大容量重合物リチウムイオン電池包装機10の第3の視野角の模式図であり、図7は、図6における局部VIIの拡大図である。図4から図7を参照すると、本実施例による大容量重合物リチウムイオン電池包装機10は、基盤100と、基盤100に設けられる支持フレーム110と、基盤100に設けられるパッケージング機構と、搬送機構と、搬送機構に伝動可能に接続されるセル治具とを含む。本実施例では、パッケージング機構は、間隔をあけて設けられた1対の上パッケージング機構120と、間隔をあけて設けられた1対の下パッケージング機構122と、第1の昇降機構124とを含み、上パッケージング機構120と下パッケージング機構122とは、いずれも成形装置130(図1、図2を参照)を含む。上パッケージング機構120は、下パッケージング機構122の直上に位置し、上パッケージング機構120は、支持フレーム110に取り付けられ、上パッケージング機構120の成形ブロック138(図1、図2を参照)と下パッケージング機構122の成形ブロック138とは、高さ方向において間隔をもって対向する。
<Example>
Fig. 4 is a schematic diagram of a first viewing angle of the
図1は、本発明の実施例による成形装置130の第1の視野角の模式図であり、図2は、本発明の実施例による成形装置130の第2の視野角の模式図であり、図3は、図1における局部IIIの拡大図である。図1から図3を参照すると、本実施例の成形装置130は、重ねて設けられる第1の固定板131、第2の固定板132、及び、成形ブロック138を含む。第1の固定板131と第2の固定板132とは、第1のボルト133によって接続される。第2のボルト134は、第2の固定板132の第1の固定板131から離れた側から第2の固定板132を貫通して第1の固定板131と第2の固定板132との間に挿入される。成形ブロック138は、第2の固定板132の第1の固定板131から離れた側に固定され、成形ブロック138には、成形ブロック138に熱を加えるための加熱装置(未図示)が設けられている。本発明では、第1のボルト133は、2つの固定板に互いに接近させる予締力を提供することによって、締め付けることができる。一方、第2のボルト134の端部は、第1の固定板131に当接することで、ねじ締める時に2つの固定板に互いに離間させる予締力を提供することができる。第1のボルト133と第2のボルト134とを調節することにより、第2の固定板132の第1の固定板131に対する位置を調整することができる。このように、第2の固定板132が変形し又は平行度が比較的悪い場合、成形ブロック138が上記調整により良好な平行度を得られ、パッケージング効果を改善することができる。
1 is a schematic diagram of a first viewing angle of a
本実施例では、第1の固定板131と成形ブロック138とは、選択的に電池の側辺をシーリングするためのストリップ状のものである。成形ブロック138の材料は金属であり、選択的に真鍮、紫銅又はステンレス鋼などであり、加熱装置は、選択的に成形ブロック138に熱を加えるための電気加熱装置である。一定温度とされた2つの成形ブロック138は、セル160の上下の2枚のパッケージング材料(例えば、アルミプラスチックフィルム)の辺縁部を挟持して溶接し、パッケージング効果を奏することができる。
In this embodiment, the
第1の固定板131が成形ブロック138の熱伝導によって過度の高温にならない断熱効果を達成するために、第1の固定板131と第2の固定板132との間には、さらに、第1の断熱板136が設けられている。第1の断熱板136は、断熱材、例えばガラス繊維、アスベスト又は真空材などで製作される。
To achieve an insulating effect that prevents the first
さらに、第2の固定板132の第1の固定板131に向かい合う側には、調節溝が設けられており、調節溝の両側は、第2の固定板132の対向する両側に貫通し、調節溝は、第2の固定板132と第1の断熱板136との間に隙間135を形成し、第2のボルト134は、調節溝に挿入され、第1の断熱板136の表面に当接させるために用いられる。隙間135は、第2の固定板132から第1の固定板131への熱伝導をさらに低減するとともに、第2の固定板132の中間部と第1の固定板131との間の距離調整範囲をより大きくし、調整性を向上させることができる。
Furthermore, an adjustment groove is provided on the side of the second fixed
本実施例では、成形装置130は、第2の固定板132の第1の固定板131から離れた側に固定される成形ブロックベース137をさらに含み、成形ブロック138は、成形ブロックベース137と固定的に接続される。接続の方式は、ボルトなどの締結部材による接続、接着又は磁気吸引による接続であってもよい。本実施例では、図2に示すように、成形ブロックベース137の長手方向に垂直な断面形状は、ほぼL字状を呈し、成形ブロック138は、成形ブロックベース137の内側の角部の両側壁に密着して取り付けられる。熱伝導を減少するために、第2の固定板132と成形ブロックベース137との間には、第2の断熱板139が設けられており、第2の断熱板139の材料は、第1の断熱板136と同じであってもよい。組み立てを容易にするために、第1の固定板131、第2の固定板132、第1の断熱板136、第2の断熱板139及び成形ブロックベース137は、成形ブロック138の長手方向において両端が面一となっており、調節溝は、成形ブロック138の長手方向に垂直な方向において第2の固定板132の両側を貫通する。
In this embodiment, the
本実施例では、複数の第1のボルト133と複数の第2のボルト134とは、成形ブロック138の長手方向において間隔をあけて交互に並べられ、間隔をあけて2列に配置される。即ち、2列のボルトは、成形ブロック138の幅方向において間隔をあけて取り付けられ、成形ブロック138の長手方向に沿って延在する。
In this embodiment, the
本実施例では、成形装置130の第2の固定板132、第1の断熱板136、第2の断熱板139及び成形ブロックベース137は、いずれも複数セグメントがあり、且つ、成形ブロック138の長手方向において並んで順次に配列され、複数の第2の固定板132は、複数の第2の断熱板139及び成形ブロックベース137を介してともに同一の成形ブロック138に接続される。即ち、成形ブロック138の長さは、並べられた複数の成形ブロックベース137の全長と略等しい。本実施例では、第2の固定板132、第1の断熱板136、第2の断熱板139及び成形ブロックベース137は、いずれも3つのセグメントに分割され、対応する第2の固定板132、第1の断熱板136、第2の断熱板139及び成形ブロックベース137の両端は面一となる。即ち、セグメントごとに第2の固定板132、第1の断熱板136、第2の断熱板139及び成形ブロックベース137は、すべて1対1に対応している。本発明の他の実施例では、パッケージングしようとする電池サイズに応じて、分割されるセグメント数及び成形ブロックの長さを調整してもよい。
In this embodiment, the second fixed
図4を参照すると、第1の昇降機構124は、基盤100の上の支持フレーム110に設けられ、第1の昇降機構124は、上パッケージング機構120を下パッケージング機構122に対して接近させる、又は、離間させるように駆動することで、上パッケージング機構120の成形ブロック138と下パッケージング機構122の成形ブロック138とを当接させる、又は、離間させる。上パッケージング機構120の成形ブロック138と下パッケージング機構122の成形ブロック138とは、加熱状態で互いに接近して当接することで、セル160辺縁部のアルミプラスチックフィルムを挟持して溶接し、パッケージング効果を奏する。本実施例の2つの上パッケージング機構120と2つの下パッケージング機構122とは、一回でセル160の両側のアルミプラスチックフィルムを溶接することができる。
Referring to FIG. 4, the
本実施例では、第1の昇降機構124は、支持フレーム110に設けられる複数の昇降シリンダを含み、上パッケージング機構120は、第1の昇降ガイドバー123をさらに含み、第1の昇降ガイドバー123の一端は、上パッケージング機構120の第1の固定板131に接続され、上パッケージング機構120の昇降方向に沿って延在する。第1の昇降ガイドバー123は、支持フレーム110の貫通孔を貫通する。このような設計によれば、上パッケージング機構120は、昇降中に鉛直方向に沿う動きを安定して維持することができ、水平方向に揺れてパッケージング効果に影響を与えにくくなる。
In this embodiment, the
図4及び図5を参照すると、搬送機構は、スクリュー142と、ガイドレール140と、スクリュー142の回動を駆動するための駆動部144とを含む。本実施例では、搬送機構は、平行して間隔をあけた2本のガイドレール140を含み、ガイドレール140は、基盤100に設けられる。スクリュー142は、2本のガイドレール140の間に位置し、その一端が、基盤100の一端に設けられる駆動部144と伝動可能に接続され、その他端が、基盤100の他端の1つの取り付け座に回動可能に接続される。スクリュー142の延在方向は、ガイドレール140の延在方向と一致する。セル治具は、スクリュー142とねじ接続されるとともに、ガイドレール140とスライド可能に接続され、これにより、駆動部144は、セル治具がセル160を運んでガイドレール140に沿って動くように当該セル治具を駆動することができる。ガイドレール140の一部は、パッケージング機構内に進入し、セル160は、搬送機構によって上パッケージング機構120と下パッケージング機構122との間に搬入され、そして、パッケージング化された後に搬出される。本実施例では、駆動部144は、選択的にステッピングモータであり、外部電源に接続される。
4 and 5, the conveying mechanism includes a
セル治具は、セル160を固定するために用いられ、セル治具は、基板150と、セル160を載置するための載置板151と、セル160を押圧するための押圧機構152と、第2の昇降機構154とを含む。本実施例では、基板150の下側には、スクリュー142と嵌め合うナットを設け、基板150は2本のガイドレール140に対してスライド可能に組み合わせられる。基板150の幅が2つの下パッケージング機構122の間の距離よりも小さいため、基板150は、2つの下パッケージング機構122の間に位置する。載置板151は、第2の昇降機構154を介して、基板150の上方に接続される。本実施例では、第2の昇降機構154は、シリンダであり、載置板151の下面には、載置板151に垂直な4つの第2の昇降ガイドバー155が設けられ、第2の昇降ガイドバー155は、基板150の4つの貫通孔に挿入されて基板150とスライド可能に接続されることで、載置板151は、昇降時に左右に揺れることなく安定して鉛直方向における動きを維持できる。
The cell jig is used to fix the
さらに、載置板151の幅は、2つの下パッケージング機構122の成形ブロック138の間の距離よりも大きい。載置板151には、下パッケージング機構122の成形ブロック138を通過させるための1対の逃げ溝156(図7を参照)が設けられている。載置板151がセル160を搭載して下パッケージング機構122の上方まで移動すると、載置板151が降下し、下パッケージング機構122の成形ブロック138は、下から上へ逃げ溝156を通過してセル160の両側のシーリングすべき位置に到着する。この時、上パッケージング機構120が降下して、下パッケージング機構122と合わさり、セル160の両側のアルミプラスチックフィルムのシーリングを完成する。
Furthermore, the width of the mounting
本実施例では、載置板151の一方側には、2つの位置決めブロック153が設けられる。位置決めブロック153は、セル160を位置決めするようにセル160の極タブを挟持するために用いられる。押圧機構152は、載置板151の上方に設けられる押圧シリンダであり、押圧シリンダは、セル160を下へ押圧することで、セル160を載置板151の上面にしっかりと固定する。
In this embodiment, two
大容量重合物リチウムイオン電池包装機10の稼働フローは、以下のとおりである。
The operating flow of the large-capacity polymer lithium-ion
作業員は、まず、パッケージングしようとするセル160を載置板151上に置き、2つの位置決めブロック153によりセル160を位置決めし、そして、押圧機構152によりセル160を押圧する。搬送機構の駆動部144を起動して、セル160の治具をパッケージング領域へ動かし、パッケージング位置に正確に到着させた後に、第2の昇降機構154により、載置板151を降下させ、セル160の下層のアルミプラスチックフィルムを下パッケージング機構122の成形ブロック138の表面に運搬する。次に、第1の昇降機構124を起動して2つの上パッケージング機構120を降下させ、上パッケージング機構120と下パッケージング機構122の成形ブロック138とを合わせてセル160の上下層のアルミプラスチックフィルムを押圧して溶接し、パッケージングプロセスを完了させる。パッケージングが完了した後、上パッケージング機構120を上昇させ、第2の昇降機構154により、載置板151を上昇させてセル160を持ち上げ、下パッケージング機構122の成形ブロック138から離脱させる。搬送機構の駆動部144を再起動し、セル160をパッケージング領域から引き離す。次に、作業員は、パッケージングされたセル160を取り出す。
The worker first places the
以上のように、本発明の実施例による大容量重合物リチウムイオン電池包装機10は、間隔をあけて設けられた少なくとも1対の上パッケージング機構120と間隔をあけて設けられた少なくとも1対の下パッケージング機構122と、第1の昇降機構124と、セル160を固定するためのセル治具と、セル治具と伝動可能に接続される搬送機構とを含む。上パッケージング機構120と下パッケージング機構122とは、いずれも成形装置130を含み、成形装置130は、パッケージング材料を溶接するための成形ブロック138を含み、上パッケージング機構120の成形ブロック138と下パッケージング機構122の成形ブロック138とは、高さ方向において間隔を持って対向する。第1の昇降機構124は、上パッケージング機構120の成形ブロック138と下パッケージング機構122の成形ブロック138とを当接させる、又は、離間させるように、上パッケージング機構120を下パッケージング機構122に対して接近させる、又は、離間させるように駆動するために用いられる。上パッケージング機構120と下パッケージング機構122の成形ブロック138とが当接する時に、アルミプラスチックフィルムを溶接してパッケージング効果を実現することができる。搬送機構は、セル治具を上パッケージング機構120と下パッケージング機構122との間に搬入するために用いられる。本発明の大容量重合物リチウムイオン電池包装機10は、セル160の挟持、搬送、パッケージングの機能を実現でき、電池のパッケージング効率を大幅に向上させることができる。
As described above, the large-capacity polymer lithium-ion
以上は本発明の好ましい実施例に過ぎず、本発明を制限するものではなく、当業者にとって、本発明は、様々な変更及び変化が可能である。本発明の精神及び原則内で行われた任意の修正、同等の置換、改良などはいずれも本発明の保護範囲内に含まれるべきである。 The above is merely a preferred embodiment of the present invention, and is not intended to limit the present invention. Those skilled in the art will appreciate that the present invention may be modified and changed in various ways. Any modifications, equivalent replacements, improvements, etc. made within the spirit and principles of the present invention should be included within the scope of protection of the present invention.
10 大容量重合物リチウムイオン電池包装機
100 基盤
110 支持フレーム
120 上パッケージング機構
122 下パッケージング機構
123 第1の昇降ガイドバー
124 第1の昇降機構
130 成形装置
131 第1の固定板
132 第2の固定板
133 第1のボルト
134 第2のボルト
135 隙間
136 第1の断熱板
137 成形ブロックベース
138 成形ブロック
140 ガイドレール
142 スクリュー
144 駆動部
150 基板
151 載置板
152 押圧機構
153 位置決めブロック
154 第2の昇降機構
155 第2の昇降ガイドバー
156 逃げ溝
160 セル
10 Large-capacity polymer lithium-ion
Claims (10)
第1の昇降機構と、
セルを固定するためのセル治具と、
前記セル治具と伝動可能に接続され、前記セル治具を前記上パッケージング機構と前記下パッケージング機構との間に搬入するための搬送機構と、を含み、
前記上パッケージング機構及び前記下パッケージング機構は、それぞれ、パッケージング材料を溶接するための成形ブロックを有する成形装置を備え、前記上パッケージング機構の成形ブロックと前記下パッケージング機構の成形ブロックとは、高さ方向において間隔を持って対向し、
前記第1の昇降機構は、前記上パッケージング機構の成形ブロックと前記下パッケージング機構の成形ブロックとを当接させる、又は、離間させるために、前記上パッケージング機構を前記下パッケージング機構に対して接近させる、又は、離間させるように駆動する、大容量重合物リチウムイオン電池包装機。 at least one pair of spaced apart upper packaging mechanisms and at least one pair of spaced apart lower packaging mechanisms;
A first lifting mechanism;
a cell jig for fixing the cell;
a transport mechanism that is operably connected to the cell jig and that transports the cell jig between the upper packaging mechanism and the lower packaging mechanism;
the upper packaging mechanism and the lower packaging mechanism each include a molding device having a molding block for welding a packaging material, the molding block of the upper packaging mechanism and the molding block of the lower packaging mechanism face each other with a gap in the height direction;
A large-capacity polymer lithium-ion battery packaging machine, wherein the first lifting mechanism drives the upper packaging mechanism to approach or move away from the lower packaging mechanism in order to abut or separate the forming blocks of the upper packaging mechanism and the lower packaging mechanism.
前記第1の昇降機構と前記上パッケージング機構とは、それぞれ、前記支持フレームに設けられ、前記上パッケージング機構は、第1の昇降ガイドバーをさらに含み、前記第1の昇降ガイドバーの一端は、前記上パッケージング機構の第1の固定板に接続されるとともに、前記上パッケージング機構の昇降方向に沿って延在し、前記第1の昇降ガイドバーは、前記支持フレームの貫通孔を貫通する、請求項1に記載の大容量重合物リチウムイオン電池包装機。 A support frame is included.
2. The large-capacity polymer lithium-ion battery packaging machine according to claim 1, wherein the first lifting mechanism and the upper packaging mechanism are each provided on the support frame, the upper packaging mechanism further includes a first lifting guide bar, one end of the first lifting guide bar is connected to a first fixed plate of the upper packaging mechanism and extends along the lifting direction of the upper packaging mechanism, and the first lifting guide bar passes through a through hole of the support frame.
2. The large-capacity polymer lithium ion battery packaging machine according to claim 1, wherein the molding block is provided with a heating device for heating the molding block.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023078515A JP2024162705A (en) | 2023-05-11 | 2023-05-11 | Large capacity polymer lithium ion battery packaging machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023078515A JP2024162705A (en) | 2023-05-11 | 2023-05-11 | Large capacity polymer lithium ion battery packaging machine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| JP2024162705A true JP2024162705A (en) | 2024-11-21 |
Family
ID=93522118
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2023078515A Pending JP2024162705A (en) | 2023-05-11 | 2023-05-11 | Large capacity polymer lithium ion battery packaging machine |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP2024162705A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119944033A (en) * | 2025-04-07 | 2025-05-06 | 济南大学 | A soft pack battery heat sealing system |
| CN121215914A (en) * | 2025-11-24 | 2025-12-26 | 江苏万历新能源有限公司 | A lithium-ion battery packaging device for automobiles |
-
2023
- 2023-05-11 JP JP2023078515A patent/JP2024162705A/en active Pending
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119944033A (en) * | 2025-04-07 | 2025-05-06 | 济南大学 | A soft pack battery heat sealing system |
| CN121215914A (en) * | 2025-11-24 | 2025-12-26 | 江苏万历新能源有限公司 | A lithium-ion battery packaging device for automobiles |
| CN121215914B (en) * | 2025-11-24 | 2026-03-06 | 江苏万历新能源有限公司 | A lithium-ion battery packaging device for automobiles |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109713351B (en) | Insulating film packaging device for secondary battery | |
| US9627706B2 (en) | Fuel-cell-stack manufacturing method and manufacturing device | |
| KR102043902B1 (en) | Electrode Stacking Device for Secondary Cell | |
| CN111545854B (en) | Assembly and welding system of battery modules | |
| KR102839255B1 (en) | Zigzag stacking apparatus for battery electrode | |
| WO2024000624A1 (en) | Busbar welding device | |
| KR102640956B1 (en) | Clamping module, clamping transfer device comprising the same, and secondary battery cell device | |
| CN111270222B (en) | TOPCon battery double-sided coating equipment | |
| KR20170117681A (en) | Taping Apparatus Capable of Attaching Adhesive Tape to Battery Cell | |
| US20240291013A1 (en) | Pouch-Type Battery Cell and Pouch Wing Bending Device of Pouch-Type Battery Cell | |
| KR101508547B1 (en) | Apparatus for heat bonding film to lead tab of secondary battery | |
| WO2024198381A1 (en) | Hot-press device | |
| KR20180068793A (en) | Device and method for bonding fuel cell part | |
| CN111571012A (en) | Photovoltaic panel processing and assembling equipment and working method thereof | |
| CN210110942U (en) | Battery cell stacking device | |
| JP2013166287A (en) | Heat sealing device and heat sealing method | |
| KR102264654B1 (en) | Ultrasonic Welding Assembly Comprising Tab Alignment Part and Ultrasonic Welding Method Using the Same | |
| AU2015297244B2 (en) | Stack welding apparatus for redox flow battery | |
| KR20180085842A (en) | Clamping Apparatus of Battery Cell Comprising Fixing Jig Employed with Guide Block for Alignment of Battery Cell | |
| CN116423134A (en) | Fuel cell bipolar plate welding tool and welding method | |
| WO2018198198A1 (en) | Workpiece transport device and workpiece transport method | |
| JP4928417B2 (en) | Electric double layer capacitor manufacturing method and manufacturing apparatus | |
| KR100901605B1 (en) | Clamping Device for Applying Fuel Cell Metal Separator Sealer | |
| CN208256823U (en) | A kind of high capacity polymer lithium ion battery sealing machine | |
| CN219215092U (en) | Intermediate positioning module stacking device and module transporting trolley |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20260421 |