JP2017055988A - Game board and production method thereof - Google Patents
Game board and production method thereof Download PDFInfo
- Publication number
- JP2017055988A JP2017055988A JP2015183314A JP2015183314A JP2017055988A JP 2017055988 A JP2017055988 A JP 2017055988A JP 2015183314 A JP2015183314 A JP 2015183314A JP 2015183314 A JP2015183314 A JP 2015183314A JP 2017055988 A JP2017055988 A JP 2017055988A
- Authority
- JP
- Japan
- Prior art keywords
- game board
- adhesive
- layer
- decorative
- transparent
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 52
- 239000011888 foil Substances 0.000 claims abstract description 163
- 239000012790 adhesive layer Substances 0.000 claims abstract description 111
- 230000001681 protective effect Effects 0.000 claims abstract description 107
- 238000005520 cutting process Methods 0.000 claims abstract description 54
- 230000002093 peripheral effect Effects 0.000 claims abstract description 42
- 238000005034 decoration Methods 0.000 claims abstract description 32
- 239000010410 layer Substances 0.000 claims description 191
- 230000001070 adhesive effect Effects 0.000 claims description 166
- 239000000853 adhesive Substances 0.000 claims description 156
- 239000000463 material Substances 0.000 claims description 82
- 238000007639 printing Methods 0.000 claims description 73
- 238000000034 method Methods 0.000 claims description 67
- 230000008569 process Effects 0.000 claims description 56
- 238000000926 separation method Methods 0.000 claims description 53
- 238000012546 transfer Methods 0.000 claims description 35
- 229920000139 polyethylene terephthalate Polymers 0.000 claims description 33
- 239000005020 polyethylene terephthalate Substances 0.000 claims description 33
- 239000004820 Pressure-sensitive adhesive Substances 0.000 claims description 31
- 238000003825 pressing Methods 0.000 claims description 31
- 230000000694 effects Effects 0.000 claims description 26
- 229920005668 polycarbonate resin Polymers 0.000 claims description 25
- 239000004431 polycarbonate resin Substances 0.000 claims description 25
- 239000004925 Acrylic resin Substances 0.000 claims description 23
- 229920000178 Acrylic resin Polymers 0.000 claims description 23
- 229920005992 thermoplastic resin Polymers 0.000 claims description 21
- 230000005856 abnormality Effects 0.000 claims description 15
- 239000002313 adhesive film Substances 0.000 claims description 15
- 229920001225 polyester resin Polymers 0.000 claims description 14
- 239000003292 glue Substances 0.000 claims description 13
- 239000004645 polyester resin Substances 0.000 claims description 13
- 230000015572 biosynthetic process Effects 0.000 claims description 8
- -1 polyethylene terephthalate Polymers 0.000 claims description 6
- 229920000728 polyester Polymers 0.000 claims description 5
- 239000010408 film Substances 0.000 description 254
- 239000000976 ink Substances 0.000 description 65
- 229920000515 polycarbonate Polymers 0.000 description 30
- 239000004417 polycarbonate Substances 0.000 description 30
- NIXOWILDQLNWCW-UHFFFAOYSA-N acrylic acid group Chemical group C(C=C)(=O)O NIXOWILDQLNWCW-UHFFFAOYSA-N 0.000 description 26
- 229910001220 stainless steel Inorganic materials 0.000 description 25
- 239000010935 stainless steel Substances 0.000 description 25
- 238000013461 design Methods 0.000 description 16
- 239000000758 substrate Substances 0.000 description 14
- 239000010409 thin film Substances 0.000 description 13
- 229920005989 resin Polymers 0.000 description 9
- 239000011347 resin Substances 0.000 description 9
- 238000007645 offset printing Methods 0.000 description 7
- 239000004973 liquid crystal related substance Substances 0.000 description 6
- 230000007246 mechanism Effects 0.000 description 6
- 239000004743 Polypropylene Substances 0.000 description 5
- 229920001155 polypropylene Polymers 0.000 description 5
- 238000004080 punching Methods 0.000 description 5
- 238000004804 winding Methods 0.000 description 5
- 239000003522 acrylic cement Substances 0.000 description 4
- 239000000126 substance Substances 0.000 description 4
- 230000000087 stabilizing effect Effects 0.000 description 3
- 238000007740 vapor deposition Methods 0.000 description 3
- 239000002699 waste material Substances 0.000 description 3
- 101100008048 Caenorhabditis elegans cut-4 gene Proteins 0.000 description 2
- BZHJMEDXRYGGRV-UHFFFAOYSA-N Vinyl chloride Chemical compound ClC=C BZHJMEDXRYGGRV-UHFFFAOYSA-N 0.000 description 2
- 239000003086 colorant Substances 0.000 description 2
- 239000000428 dust Substances 0.000 description 2
- 238000009864 tensile test Methods 0.000 description 2
- 238000012360 testing method Methods 0.000 description 2
- 230000037303 wrinkles Effects 0.000 description 2
- 239000012461 cellulose resin Substances 0.000 description 1
- 238000011109 contamination Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 238000010030 laminating Methods 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000004800 polyvinyl chloride Substances 0.000 description 1
- 229920000915 polyvinyl chloride Polymers 0.000 description 1
- 230000002265 prevention Effects 0.000 description 1
- 238000007790 scraping Methods 0.000 description 1
- 238000003756 stirring Methods 0.000 description 1
- 229920003002 synthetic resin Polymers 0.000 description 1
- 239000000057 synthetic resin Substances 0.000 description 1
- 238000013518 transcription Methods 0.000 description 1
- 230000035897 transcription Effects 0.000 description 1
Images










Landscapes
- Pinball Game Machines (AREA)
Abstract
Description
本発明は、パチンコ遊技機、アレンジボール遊技機、回胴式遊技機等の各種遊技機に採用される遊技盤及びその製造方法に関する。 The present invention relates to a game board employed in various game machines such as a pachinko game machine, an arrange ball game machine, and a revolving game machine, and a method for manufacturing the same.
従来、遊技機の遊技盤としては、例えば、下記特許文献1に記載の遊技機の遊技盤が提案されている。当該遊技盤は、遊技用基盤と、この遊技用基板の各開口部に設けてなるガイドレール、液晶表示装置その他の盤面部品とにより構成されている。ここで、遊技用基盤は、透光性合成樹脂盤よりなる本体盤と、各種図柄を印刷されて本体盤の前面に貼着してなる薄膜状シート材とを備えている。 Conventionally, as a gaming board of a gaming machine, for example, a gaming board of a gaming machine described in Patent Document 1 below has been proposed. The game board is composed of a game base, guide rails provided at each opening of the game board, a liquid crystal display device, and other board surface parts. Here, the game board includes a main body board made of a translucent synthetic resin board and a thin film sheet material on which various designs are printed and adhered to the front surface of the main body board.
ところで、上述した遊技機の遊技盤において、近年、遊技盤の各開口部のうち、液晶表示装置を設ける開口部の開口面積は、液晶表示装置の大型化につれて広くなっている。このため、液晶表示装置を設ける開口部の開口面積が広いと、薄膜状シート材が折れ曲がり易くなる。 By the way, in the gaming board of the gaming machine described above, in recent years, the opening area of the opening portion where the liquid crystal display device is provided among the opening portions of the gaming board has become wider as the liquid crystal display device becomes larger. For this reason, when the opening area of the opening portion in which the liquid crystal display device is provided is large, the thin-film sheet material is easily bent.
ここで、遊技用基板の各開口部は、本体盤及び薄膜状シート材の双方に共通に形成されている。このため、薄膜状シート材を本体盤の前面に貼着するにあたり、薄膜状シート材の各開口部のうち、例えば、液晶表示装置を設ける開口部を、本体盤の各開口部のうち液晶表示装置を設ける開口部に合わせて貼着しようとしても、上述のごとく、薄膜状シート材が折れ曲がり易いと、両開口部の間に位置ずれが生じて当該両開口部を正しく合わせることができなかったり、薄膜状シート材に皺が発生したりして、薄膜状シート材の本体盤に対する貼着が良好にはなされ得ないという不具合を招く。 Here, each opening part of the game board | substrate is formed in common with both a main body board and a thin film-like sheet material. For this reason, when sticking a thin film-like sheet material to the front surface of a main body board, among each opening part of a thin film-like sheet material, for example, the opening part which provides a liquid crystal display device is used for liquid crystal display Even if it is intended to be attached to the opening provided with the device, as described above, if the thin-film sheet material is likely to be bent, the opening may be misaligned between the openings, and the openings may not be properly aligned. In addition, wrinkles occur in the thin film sheet material, which causes a problem that the thin film sheet material cannot be satisfactorily adhered to the main body board.
また、薄膜状シート材の本体盤に対する貼着が良好になされたとしても、例えば、薄膜状シート材と本体盤との間にゴミが混入したり、或いは、薄膜状シート材及び本体盤の一方が貼り合わせる対象として誤っていたりした場合、薄膜状シート材を本体盤から剥がして、本体盤の再利用を確保しつつ当該本体盤に新たな薄膜状シート材を貼着し直したいという要請が生ずる。この場合、薄膜状シート材の本体盤に対する貼着後、薄膜状シート材を本体盤から良好に剥がせないと、本体盤の再利用は困難である。 Further, even if the thin film sheet material is successfully adhered to the main body board, for example, dust is mixed between the thin film sheet material and the main body board, or one of the thin film sheet material and the main body board is mixed. If there is a mistake in attaching the thin film sheet material to the main body board, a request to reattach the new thin film sheet material to the main body board is ensured while ensuring reuse of the main body board. Arise. In this case, it is difficult to reuse the main body board unless the thin film sheet material can be satisfactorily peeled from the main body board after the thin film sheet material is attached to the main body board.
さらに、上述した遊技盤の薄膜状シート材における加飾は、単に印刷された各種図柄によるものであるため、ありふれた表現しかできず、見映えしなかった。従って、新しい斬新な加飾によるさらなる斬新な表現力の向上が望まれている。 Furthermore, the decoration on the thin film sheet material of the above-described game board is simply based on various printed patterns, so that it can only be expressed as usual and did not look good. Accordingly, there is a demand for further improvement of the expressive power by new and innovative decoration.
そこで、本発明は、以上のようなことに対処するため、化粧シートの遊技基板に対する貼り直しが必要なときには、当該化粧シートを遊技基板から剥がした後において当該遊技基板に対する新たな化粧シートの良好な貼り直しを可能にしつつ、新しい加飾による見映えのさらなる向上も可能にするようにした遊技盤及びその製造方法を提供することを目的とする。 Therefore, in order to deal with the above, the present invention provides a new decorative sheet for the game board after the decorative sheet is peeled off from the game board when it is necessary to reattach the decorative sheet to the game board. It is an object of the present invention to provide a game board and a method for manufacturing the same, which enable further reappearance and further improve the appearance by new decoration.
上記課題の解決にあたり、本発明に係る遊技盤は、請求項1の記載によれば、パチンコ遊技機の各種遊技部品を組み付けるための遊技基板(10)及び化粧シート(S)を粘着層(30)を介して貼着してなる遊技盤である。 In solving the above-described problems, according to the gaming board according to the present invention, the gaming board (10) and the decorative sheet (S) for assembling various gaming parts of the pachinko gaming machine are attached to the adhesive layer (30 ) Is a game board that is pasted through.
当該遊技盤においては、
遊技基板は、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)であり、
化粧シートは、その裏面に所定の図柄(22)が形成された後、当該裏面の一部に印刷された、ホログラム箔を付着させるための透明な特殊インク(24)を介してホログラム箔(25)が転写されたものであり、
粘着層は、遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなるものである。
In the game board,
The game board is a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts.
The decorative sheet has a predetermined pattern (22) formed on the back surface thereof, and then is printed on a hologram foil (25) via a transparent special ink (24) printed on a part of the back surface for attaching the hologram foil. ) Is transcribed,
When the adhesive layer is attached to the surface of the game board, the adhesive layer is a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. It is formed.
このような粘着層を形成する粘着剤の特性により、化粧シートを遊技基板に貼着した短時間内であれば、遊技基板に対する化粧シートの粘着力は低い。従って、化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板からきれいに剥がすことができる。これに伴い、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板の再利用が可能となる。 Due to the characteristics of the pressure-sensitive adhesive forming such a pressure-sensitive adhesive layer, the adhesive strength of the decorative sheet to the game board is low within a short time after the decorative sheet is stuck to the game board. Therefore, when an abnormality of the decorative sheet or a foreign substance is found between the adhesive layer and the game board, the decorative sheet can be removed cleanly from the game board. Accordingly, it becomes possible to reuse a game board made of expensive polycarbonate resin or acrylic resin.
さらに、化粧シートには、従来の化粧シートと同様な図柄の形成に加え、ホログラム箔も転写されているので、従来の図柄による加飾に加え、ホログラム箔による新しい加飾、具体的には、レーザー光線がホログラム箔に照射され、ホログラム箔の柄が浮き出るといった新しい加飾による見映えのさらなる向上を図ることが可能となる。 Furthermore, in addition to the formation of the same design as the conventional decorative sheet, the hologram foil is also transferred to the decorative sheet, so in addition to the traditional decorative decoration, a new decorative decorative foil, specifically, It is possible to further improve the appearance by a new decoration such that the hologram foil is irradiated with the laser beam and the pattern of the hologram foil is raised.
また、本発明に係る遊技盤は、請求項2の記載によれば、パチンコ遊技機の各種遊技部品を組み付けるための遊技基板(10)及び化粧シート(S)を粘着層(30)を介して貼着してなる遊技盤である。 According to the second aspect of the game board according to the present invention, the game board (10) and the decorative sheet (S) for assembling various game parts of the pachinko gaming machine are provided via the adhesive layer (30). It is a game board that is attached.
当該遊技盤においては、
遊技基板は、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)であり、
化粧シートは、その裏面に所定の図柄(22)が形成された後、当該裏面の一部に印刷された、ホログラム箔を付着させるための透明な第1特殊インク(24)を介してホログラム箔(25)が転写され、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インク(26)が印刷にて流し込まれたものであり、
粘着層は、遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなるものである。
In the game board,
The game board is a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts.
The decorative sheet has a predetermined pattern (22) formed on the back surface thereof, and then is printed on a part of the back surface through a transparent first special ink (24) for adhering the hologram foil. (25) is transferred, and the hologram foil is not transferred in order to fill the level difference between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred to flatten the surface. A transparent second special ink (26) is poured into the part by printing,
When the adhesive layer is attached to the surface of the game board, the adhesive layer is a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. It is formed.
このような粘着層を形成する粘着剤の特性により、化粧シートを遊技基板に貼着した短時間内であれば、遊技基板に対する化粧シートの粘着力は低い。従って、化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板からきれいに剥がすことができる。これに伴い、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板の再利用が可能となる。 Due to the characteristics of the pressure-sensitive adhesive forming such a pressure-sensitive adhesive layer, the adhesive strength of the decorative sheet to the game board is low within a short time after the decorative sheet is stuck to the game board. Therefore, when an abnormality of the decorative sheet or a foreign substance is found between the adhesive layer and the game board, the decorative sheet can be removed cleanly from the game board. Accordingly, it becomes possible to reuse a game board made of expensive polycarbonate resin or acrylic resin.
さらに、化粧シートには、従来の化粧シートと同様な図柄の形成に加え、ホログラム箔も転写されているので、従来の図柄による加飾に加え、ホログラム箔による新しい加飾、具体的には、レーザー光線がホログラム箔に照射され、ホログラム箔の柄が浮き出るといった新しい加飾による見映えのさらなる向上を図ることが可能となる。 Furthermore, in addition to the formation of the same design as the conventional decorative sheet, the hologram foil is also transferred to the decorative sheet, so in addition to the traditional decorative decoration, a new decorative decorative foil, specifically, It is possible to further improve the appearance by a new decoration such that the hologram foil is irradiated with the laser beam and the pattern of the hologram foil is raised.
また、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差が埋まって、その表面がフラットになっているので、盤面がフラットでなければならないという規定に適正に対処することができる。 In addition, the level difference between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred is filled and the surface is flat, so that the board surface must be flat. Can be dealt with.
また、本発明は、請求項3の記載によれば、請求項1または2に記載の遊技盤において、上記所定の雰囲気温度は、粘着層が遊技基板に対する粘着力を良好に発揮し得る温度であるようにしてもよい。 According to a third aspect of the present invention, in the game board according to the first or second aspect, the predetermined atmospheric temperature is a temperature at which the adhesive layer can satisfactorily exert an adhesive force to the game board. There may be.
上記課題の解決にあたり、本発明に係る遊技盤の製造方法は、請求項4の記載によれば、パチンコ遊技機の各種遊技部品を組み付けるための遊技基板及び化粧シートを用いて製造する方法である。 In solving the above-described problems, a game board manufacturing method according to the present invention is a method of manufacturing using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine according to claim 4. .
当該遊技盤の製造方法においては、
遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)を予め準備し、
かつ、当該遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層(30)を予め準備する。
In the manufacturing method of the game board,
As a game board, a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts is prepared in advance. And
And when it is attached to the surface of the game board, it is formed with a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. An adhesive layer (30) is prepared in advance.
そして、第1熱可塑性樹脂製の保護フィルム(21)を、その裏面にて、粘着層と共に化粧シートを構成する透明の第2熱可塑性樹脂製の加飾フィルム部材(20)にその表面にて貼着する第1工程と、
当該第1工程における上記貼着後、加飾フィルム部材の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な特殊インクを印刷し、当該特殊インクの印刷された部分にホログラム箔を転写させる第2工程と、
粘着層を加飾フィルム部材にその裏面側から貼着する第3工程と、
粘着層、加飾フィルム部材及び保護フィルムからなる貼着体を、その遊技基板の上記開口部の内周面に対応する切り込み位置にて、保護フィルムを除き粘着層から加飾フィルム部材にかけて切り込み、切り込み貼着体として形成する第4工程と、
上記切り込み貼着体を、その粘着層にて、遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
保護フィルムを加飾フィルム部材から剥がしながら、上記切り込み貼着体のうち上記切り込み位置の内側部位を保護フィルムと共に一体的に除去する第6工程とを備えて、
上記第1〜第6の工程を上記所定の雰囲気温度の環境内で行い、上記第6工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に上記第1〜第6の工程を経て貼着し直すことで製造するようにしたことを特徴とする。
And the protective film (21) made from a 1st thermoplastic resin is on the surface in the transparent film decoration film member (20) made from a 2nd thermoplastic resin which comprises a decorative sheet with an adhesion layer in the back surface. The first step to stick,
After the pasting in the first step, a predetermined pattern is formed on the back surface of the decorative film member, and a transparent special ink for attaching the hologram foil is printed on a part of the back surface. A second step of transferring the hologram foil to the printed portion;
A third step of attaching the adhesive layer to the decorative film member from the back side;
Adhesive layer consisting of an adhesive layer, a decorative film member, and a protective film is cut from the adhesive layer to the decorative film member except for the protective film at a cutting position corresponding to the inner peripheral surface of the opening of the game board, A fourth step of forming as a cut and stuck body;
A fifth step in which the cut and stuck body is adhered to the surface of the game board with a pressure within a predetermined pressure range by using the adhesive layer;
A sixth step of integrally removing the inner part of the cut position together with the protective film while peeling off the protective film from the decorative film member,
The above first to sixth steps are performed in the environment of the predetermined atmospheric temperature, and an abnormality of the decorative sheet or the inclusion of foreign matter between the adhesive layer and the game board is found within a predetermined short time after the sixth step. When this is done, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to sixth steps to manufacture the decorative sheet.
このように、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板を活用して、第1〜第6の工程を所定の雰囲気温度の環境内で行い、第6工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に第1〜第6の工程を経て貼着し直すことで製造するようにした。 In this way, utilizing the gaming substrate made of expensive polycarbonate resin or acrylic resin, the first to sixth steps are performed in an environment of a predetermined atmospheric temperature, and the decorative sheet is within a predetermined short time after the sixth step. When an abnormality is detected or foreign matter is mixed between the adhesive layer and the game board, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to sixth steps. It was made to manufacture.
ここで、第6工程後所定の短時間内であれば,遊技基板に対する化粧シートの粘着力は低い。従って、化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板からきれいに剥がすことができる。これに伴い、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板の再利用が可能となる。 Here, the adhesive strength of the decorative sheet to the game board is low within a predetermined short time after the sixth step. Therefore, when an abnormality of the decorative sheet or a foreign substance is found between the adhesive layer and the game board, the decorative sheet can be removed cleanly from the game board. Accordingly, it becomes possible to reuse a game board made of expensive polycarbonate resin or acrylic resin.
従って、新たな化粧シートを遊技基板に第1〜第6の工程を経て良好に貼着し直すことが可能となる。このように、高価な遊技基板の再利用でもって無駄を無くすることで、省資源に貢献し得る。 Therefore, a new decorative sheet can be satisfactorily adhered to the game board through the first to sixth steps. In this way, it is possible to contribute to resource saving by eliminating waste by reusing expensive game boards.
さらに、化粧シートには、従来の化粧シートと同様な図柄の形成に加え、ホログラム箔も転写されているので、従来の図柄による加飾に加え、ホログラム箔による新しい加飾、具体的には、レーザー光線がホログラム箔に照射され、ホログラム箔の柄が浮き出るといった新しい加飾による見映えのさらなる向上を図ることが可能となる。 Furthermore, in addition to the formation of the same design as the conventional decorative sheet, the hologram foil is also transferred to the decorative sheet, so in addition to the traditional decorative decoration, a new decorative decorative foil, specifically, It is possible to further improve the appearance by a new decoration such that the hologram foil is irradiated with the laser beam and the pattern of the hologram foil is raised.
また、本発明は、請求項5の記載によれば、請求項4に記載の遊技盤の製造方法において、
上記第2工程では、転写面に糊が付いているホログラム箔を転写させる場合には、上記所定の図柄の形成後、上前記透明な特殊インクの印刷前に、当該裏面全体に亘って、ホログラム箔の定着を防止するための透明な特殊インクを印刷することを特徴とする。
According to the fifth aspect of the present invention, in the method for manufacturing a game board according to the fourth aspect,
In the second step, when transferring the hologram foil with glue on the transfer surface, the hologram is formed on the entire back surface after the predetermined pattern is formed and before the transparent special ink is printed. It is characterized by printing a transparent special ink for preventing fixing of the foil.
これにより、ホログラム箔を転写させたい部分以外には、ホログラム箔は定着しないので、製造者の意図通りの場所にホログラム箔を転写することができる。 Thereby, since the hologram foil is not fixed except for the portion where the hologram foil is to be transferred, the hologram foil can be transferred to a place as intended by the manufacturer.
また、本発明は、請求項6の記載によれば、請求項4または5に記載の遊技盤の製造方法において、
上記第2工程では、ホログラム箔を付着させるための透明な特殊インクを印刷するときには、ホログラム箔の転写を安定させるために、当該加飾フィルム部材の外周に沿って帯状の領域を印刷し、
上記第4工程では、当該切り込みと併せて、ホログラム箔が転写された上記帯状の領域を含む領域を当該加飾フィルム部材から切断して、上記切り込み貼着体の外周面形状を遊技基板の外周面形状に合わせることを特徴とする。
According to a sixth aspect of the present invention, in the game board manufacturing method according to the fourth or fifth aspect,
In the second step, when printing a transparent special ink for adhering the hologram foil, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fourth step, an area including the band-shaped area to which the hologram foil has been transferred is cut from the decorative film member in combination with the cut, and the outer peripheral surface shape of the cut and stuck body is changed to the outer periphery of the game board. It is characterized by matching to the surface shape.
これにより、ホログラム箔の転写を安定して行うことができる。そして、上記帯状の領域は、転写を安定させる目的のためだけに印刷され、ホログラム箔が転写された後は不要なものであるが、第4工程により、当該切り込みと併せて自動的に、加飾フィルム部材から切断されるので、製造者がわざわざ削除しなければならいという手間を省くことができる。 As a result, the hologram foil can be stably transferred. The band-like area is printed only for the purpose of stabilizing the transfer, and is unnecessary after the hologram foil is transferred. However, in the fourth step, the band-like area is automatically added together with the notch. Since it is cut from the decorative film member, it is possible to save the trouble that the manufacturer has to delete it.
また、本発明に係る遊技盤の製造方法は、請求項7の記載によれば、パチンコ遊技機の各種遊技部品を組み付けるための遊技基板及び化粧シートを用いて製造するようにした遊技盤の製造方法において、
遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)を予め準備し、
かつ、当該遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層(30)を予め準備して、
第1熱可塑性樹脂製の保護フィルム(21)を、その裏面にて、粘着層と共に化粧シートを構成する透明の第2熱可塑性樹脂製の加飾フィルム部材(20)にその表面にて貼着する第1工程と、
当該第1工程における上記貼着後、加飾フィルム部材の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な第1特殊インクを印刷し、当該第1特殊インクの印刷された部分にホログラム箔を転写させ、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インクを印刷にて流し込む第2工程と、
粘着層を加飾フィルム部材にその裏面側から貼着する第3工程と、
粘着層、加飾フィルム部材及び保護フィルムからなる貼着体を、その遊技基板の上記開口部の内周面に対応する切り込み位置にて、保護フィルムを除き粘着層から加飾フィルム部材にかけて切り込み、切り込み貼着体として形成する第4工程と、
上記切り込み貼着体を、その粘着層にて、遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
保護フィルムを加飾フィルム部材から剥がしながら、上記切り込み貼着体のうち上記切り込み位置の内側部位を保護フィルムと共に一体的に除去する第6工程とを備えて、上記第6工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に上記第1〜第6の工程を経て貼着し直すことで製造するようにしたことを特徴とする。
According to a seventh aspect of the present invention, there is provided a game board manufacturing method using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine. In the method
As a game board, a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts is prepared in advance. And
And when it is attached to the surface of the game board, it is formed with a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. An adhesive layer (30) is prepared in advance,
The protective film (21) made of the first thermoplastic resin is adhered on the back surface thereof to the decorative film member (20) made of a transparent second thermoplastic resin that constitutes the decorative sheet together with the adhesive layer. A first step of
After the sticking in the first step, a predetermined pattern is formed on the back surface of the decorative film member, and a transparent first special ink for attaching the hologram foil is printed on a part of the back surface, 1. To transfer the hologram foil to the printed part of the special ink, and to fill the level difference between the part where the hologram foil is transferred and the part where the hologram foil is not transferred to make the surface flat. A second step of pouring a transparent second special ink into a portion where the hologram foil is not transferred;
A third step of attaching the adhesive layer to the decorative film member from the back side;
Adhesive layer consisting of an adhesive layer, a decorative film member, and a protective film is cut from the adhesive layer to the decorative film member except for the protective film at a cutting position corresponding to the inner peripheral surface of the opening of the game board, A fourth step of forming as a cut and stuck body;
A fifth step in which the cut and stuck body is adhered to the surface of the game board with a pressure within a predetermined pressure range by using the adhesive layer;
And a sixth step of integrally removing the inner portion of the cut position together with the protective film while peeling off the protective film from the decorative film member, and a predetermined short time after the sixth step. When an abnormality of the decorative sheet or contamination of foreign matter is found between the adhesive layer and the game board, the first to sixth steps are applied to the game board by removing the decorative sheet from the game board. It is characterized in that it is manufactured by re-attaching after that.
これにより、請求項4に記載の発明と同様な作用効果を達成することに加え、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差が埋まって、その表面がフラットになっているので、盤面がフラットでなければならないという規定に適正に対処することができるという効果を奏する。 Thereby, in addition to achieving the same effect as the invention of the fourth aspect, the step formed between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred is buried, and the surface Since it is flat, there is an effect that it is possible to appropriately cope with the rule that the board surface must be flat.
また、本発明は、請求項8の記載によれば、請求項7に記載の遊技盤の製造方法において、
上記第2工程では、転写面に糊が付いているホログラム箔を転写させる場合には、上記所定の図柄の形成後、上記透明な第1特殊インクの印刷前に、当該裏面全体に亘って、ホログラム箔の定着を防止するための透明な第3特殊インクを印刷することを特徴とする。
According to the description of claim 8, the present invention provides a game board manufacturing method according to claim 7,
In the second step, when transferring the hologram foil with glue on the transfer surface, after the formation of the predetermined pattern, before printing the transparent first special ink, over the entire back surface, It is characterized by printing a transparent third special ink for preventing the hologram foil from being fixed.
これにより、請求項5に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that attained by the 5th aspect can be attained.
また、本発明は、請求項9の記載によれば、請求項7または8に記載の遊技盤の製造方法において、
上記第2工程では、上記第1特殊インクを印刷するときには、ホログラム箔の転写を安定させるために、当該加飾フィルム部材の外周に沿って帯状の領域を印刷し、
上記第4工程では、当該切り込みと併せて、ホログラム箔が転写された上記帯状の領域を含む領域を当該加飾フィルム部材から切断して、上記切り込み貼着体の外周面形状を遊技基板の外周面形状に合わせることを特徴とする。
According to a ninth aspect of the present invention, in the game board manufacturing method according to the seventh or eighth aspect,
In the second step, when printing the first special ink, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fourth step, an area including the band-shaped area to which the hologram foil has been transferred is cut from the decorative film member in combination with the cut, and the outer peripheral surface shape of the cut and stuck body is changed to the outer periphery of the game board. It is characterized by matching to the surface shape.
これにより、請求項6に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that of the sixth aspect of the invention can be achieved.
また、本発明は、請求項10の記載によれば、
パチンコ遊技機の各種遊技部品を組み付けるための遊技基板及び化粧シートを用いて製造するようにした遊技盤の製造方法において、
遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)を予め準備し、
第1熱可塑性樹脂製の長手状フィルム体からなる保護フィルムロール(50)及び透明の第2熱可塑性樹脂製の長手状フィルム体からなる加飾フィルム部材ロール(40)を予め準備し、
かつ、遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤を粘着素材とする粘着素材層(81)と、当該粘着素材層の一側面に沿い貼着してなるポリエステル系樹脂製の長手状一側分離層(82)と、粘着素材層の他側面に沿い貼着してなるポリエステル系樹脂製の長手状他側分離層(83)とでもって形成したなる粘着素材ロール(80)を予め準備して、
保護フィルムロールを加飾フィルム部材ロールに沿い貼着してフィルム貼着ロール体(60)を形成する第1工程(S1)と、
上記フィルム貼着ロール体を遊技基板に対応する長さにて切断して保護フィルム(21)及び加飾フィルム部材(20)からなる貼着フィルム層(60a)として形成する第2工程(S2)と、
貼着フィルム層の加飾フィルム部材の保護フィルムとは反対側の印刷面に所定の図柄(22)を形成し、当該印刷面の一部に、ホログラム箔を付着させるための透明な特殊インク(24)を印刷し、当該特殊インクの印刷された部分にホログラム箔(25)を転写させて印刷貼着フィルム層(70)として形成する第3工程(S3)と、
粘着素材ロールからその上記一側分離層を剥がしながら上記印刷側面に沿い貼着して印刷貼着フィルム層にあわせて切断し粘着層(30)とし、保護フィルム、加飾フィルム部材、粘着層及び他側分離層からなる複層貼着体(100)として形成する第4工程(S4)と、
複層貼着体のうち遊技基板の上記開口部の内周面に対する対応部位を、保護フィルムを除き他側分離層から加飾フィルム部材にかけて切り込み、切り込み済み対応部位として形成する第5工程(S5)と、
上記切り込み済みの保護フィルム、加飾フィルム部材、粘着層及び他側分離層からなる切り込み済み複層貼着体(100a)を、他側分離層を剥がしながら、粘着層にて、遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第6工程(S6)と、
当該第6工程後、保護フィルムを加飾フィルム部材から剥がしながら、上記切り込み済み複層貼着体の加飾フィルム部材及び粘着層のうち上記切り込み済み対応部位の内側部位を保護フィルムと共に一体的に除去する第7工程(S7)とを備えて、
上記第1〜第7の工程を上記所定の雰囲気温度の環境内で行い、上記第7工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に上記第1〜第7の工程を経て貼着し直すことで製造するようにしたことを特徴とする。
According to the description of
In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As a game board, a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts is prepared in advance. And
A protective film roll (50) made of a first thermoplastic resin longitudinal film body and a decorative film member roll (40) made of a transparent second thermoplastic resin longitudinal film body are prepared in advance,
In addition, a transparent adhesive that exhibits an adhesive property that is low immediately after the attachment when it is attached to the surface of the game board and that increases with the passage of time in an environment of a predetermined atmosphere temperature and the adhesive material. Adhesive material layer (81) to be adhered, along with one side surface of the adhesive material layer, a longitudinal one-side separation layer (82) made of polyester resin, and adhered along the other side surface of the adhesive material layer Prepare in advance an adhesive material roll (80) formed with the longitudinal other side separation layer (83) made of polyester resin,
A first step (S1) for forming a film sticking roll body (60) by sticking a protective film roll along a decorative film member roll;
2nd process (S2) which cut | disconnects the said film sticking roll body by the length corresponding to a game board | substrate, and forms as a sticking film layer (60a) which consists of a protective film (21) and a decorating film member (20). When,
A transparent special ink for forming a predetermined pattern (22) on the printed surface opposite to the protective film of the decorative film member of the sticking film layer, and attaching a hologram foil to a part of the printed surface ( 24), and transferring the hologram foil (25) to the printed portion of the special ink to form a printed adhesive film layer (70) (S3);
While peeling off the one-side separation layer from the adhesive material roll, it is adhered along the printing side surface and cut along with the printed adhesive film layer to form an adhesive layer (30), a protective film, a decorative film member, an adhesive layer, and A fourth step (S4) formed as a multi-layer adhesive body (100) comprising the other side separation layer;
5th process (S5) which cut | disconnects the site | part corresponding with respect to the internal peripheral surface of the said opening part of a game board among multi-layer stickers from the other side separated layer to a decoration film member except a protective film (S5). )When,
The above-mentioned cut protective film, decorative film member, pressure-sensitive adhesive layer and other-side separation layer, the cut multilayer adhesive body (100a), while peeling the other-side separation layer, the adhesive layer, And a sixth step (S6) for sticking with pressing with a pressure within a predetermined pressure range;
After the sixth step, while peeling off the protective film from the decorative film member, the inner portion of the cut corresponding portion of the decorative film member and the adhesive layer of the cut multilayered adhesive body is integrated with the protective film. A seventh step (S7) to be removed,
The first to seventh steps are carried out in the environment of the predetermined atmospheric temperature, and an abnormality of the decorative sheet or a foreign matter mixed between the adhesive layer and the game board is found within a predetermined short time after the seventh step. When this is done, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the above first to seventh steps to manufacture the decorative sheet.
このように、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板を活用して、第1〜第7の工程を所定の雰囲気温度の環境内で行い、第7工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に前記第1〜第7の工程を経て貼着し直すことで製造するようにした。 In this way, utilizing the gaming substrate made of expensive polycarbonate resin or acrylic resin, the first to seventh steps are performed in an environment of a predetermined atmospheric temperature, and the decorative sheet is within a predetermined short time after the seventh step. Or when a foreign material is found between the adhesive layer and the game board, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to seventh steps. I made it by repairing it.
ここで、第7工程後所定の短時間内であれば,遊技基板に対する化粧シートの粘着力は低い。従って、化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板からきれいに剥がすことができる。これに伴い、高価なポリカーボネート樹脂或いはアクリル樹脂からなる遊技基板の再利用が可能となる。 Here, the adhesive strength of the decorative sheet to the game board is low within a predetermined short time after the seventh step. Therefore, when an abnormality of the decorative sheet or a foreign substance is found between the adhesive layer and the game board, the decorative sheet can be removed cleanly from the game board. Accordingly, it becomes possible to reuse a game board made of expensive polycarbonate resin or acrylic resin.
従って、化粧シートを遊技基板に第1〜第7の工程を経て良好に貼着し直すことが可能となる。このように高価な遊技基板の再利用でもって無駄を無くすることで、省資源に貢献し得る。 Therefore, it is possible to satisfactorily reattach the decorative sheet to the game board through the first to seventh steps. In this way, it is possible to contribute to resource saving by eliminating waste by reusing expensive game boards.
さらに、化粧シートには、従来の化粧シートと同様な図柄の形成に加え、ホログラム箔も転写されているので、従来の図柄による加飾に加え、ホログラム箔による新しい加飾、具体的には、レーザー光線がホログラム箔に照射され、ホログラム箔の柄が浮き出るといった新しい加飾による見映えのさらなる向上を図ることが可能となる。 Furthermore, in addition to the formation of the same design as the conventional decorative sheet, the hologram foil is also transferred to the decorative sheet, so in addition to the traditional decorative decoration, a new decorative decorative foil, specifically, It is possible to further improve the appearance by a new decoration such that the hologram foil is irradiated with the laser beam and the pattern of the hologram foil is raised.
また、本発明は、請求項11の記載によれば、請求項10に記載の遊技盤の製造方法において、
上記第3工程では、転写面に糊が付いているホログラム箔を転写させる場合には、前記所定の図柄の形成後、前記透明な特殊インクの印刷前に、当該印刷面全体に亘って、ホログラム箔の定着を防止するための透明な特殊インク(23)を印刷することを特徴とする。
According to the eleventh aspect of the present invention, in the game board manufacturing method according to the tenth aspect,
In the third step, when transferring the hologram foil having glue on the transfer surface, the hologram is formed over the entire print surface after the predetermined pattern is formed and before the transparent special ink is printed. It is characterized by printing a transparent special ink (23) for preventing the fixing of the foil.
これにより、請求項5に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that attained by the 5th aspect can be attained.
また、本発明は、請求項12の記載によれば、請求項10または11に記載の遊技盤の製造方法において、
上記第3工程では、ホログラム箔を付着させるための透明な特殊インクを印刷するときには、ホログラム箔の転写を安定させるために、当該加飾フィルム部材の外周に沿って帯状の領域(24a)を印刷し、
上記第5工程では、当該切り込みと併せて、ホログラム箔が転写された上記帯状の領域を含む領域を当該加飾フィルム部材から切断して、上記切り込み済み複層貼着体の外周面形状を遊技基板の外周面形状に合わせることを特徴とする。
According to a twelfth aspect of the present invention, in the game board manufacturing method according to the tenth or eleventh aspect,
In the third step, when printing a transparent special ink for adhering the hologram foil, a band-like region (24a) is printed along the outer periphery of the decorative film member in order to stabilize the transfer of the hologram foil. And
In the fifth step, in addition to the cut, a region including the band-shaped region to which the hologram foil has been transferred is cut from the decorative film member, and the outer peripheral surface shape of the cut multilayer adhesive body is played. It is characterized by conforming to the shape of the outer peripheral surface of the substrate.
これにより、請求項6に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that of the sixth aspect of the invention can be achieved.
また、本発明は、請求項13の記載によれば、
パチンコ遊技機の各種遊技部品を組み付けるための遊技基板及び化粧シートを用いて製造するようにした遊技盤の製造方法において、
遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する開口部(11)を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板(10)を予め準備し、
第1熱可塑性樹脂製の長手状フィルム体からなる保護フィルムロール(50)及び透明の第2熱可塑性樹脂製の長手状フィルム体からなる加飾フィルム部材ロール(40)を予め準備し、
かつ、遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤を粘着素材とする粘着素材層(81)と、当該粘着素材層の一側面に沿い貼着してなるポリエステル系樹脂製の長手状一側分離層(82)と、粘着素材層の他側面に沿い貼着してなるポリエステル系樹脂製の長手状他側分離層(83)とでもって形成したなる粘着素材ロール(80)を予め準備して、
保護フィルムロールを加飾フィルム部材ロールに沿い貼着してフィルム貼着ロール体を形成する第1工程(S1)と、
フィルム貼着ロール体を遊技基板に対応する長さにて切断して保護フィルム(21)及び加飾フィルム部材(20)からなる貼着フィルム層(60a)として形成する第2工程(S2)と、
貼着フィルム層の加飾フィルム部材の保護フィルムとは反対側の印刷面に所定の図柄(22)を形成し、当該印刷面の一部に、ホログラム箔を付着させるための透明な第1特殊インク(24)を印刷し、当該第1特殊インクの印刷された部分にホログラム箔(25)を転写させ、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インク(26)を印刷にて流し込んで印刷貼着フィルム層(71)として形成する第3工程と、
粘着素材ロールからその上記一側分離層を剥がしながら、当該粘着素材ロールの粘着素材層を印刷貼着フィルム層の加飾フィルム部材の上記印刷側面に沿い貼着して印刷貼着フィルム層にあわせて切断し粘着層(30)とし、保護フィルム、加飾フィルム部材、粘着層及び他側分離層からなる複層貼着体(100)として形成する第4工程(S4)と、
複層貼着体のうち遊技基板の上記開口部の内周面に対する対応部位を、保護フィルムを除き他側分離層から加飾フィルム部材にかけて切り込み、切り込み済み対応部位として形成する第5工程(S5)と、
上記切り込み済みの保護フィルム、加飾フィルム部材、粘着層及び他側分離層からなる切り込み済み複層貼着体(100a)を、他側分離層を剥がしながら、粘着層にて、遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第6工程(S6)と、
当該第6工程後、保護フィルムを加飾フィルム部材から剥がしながら、上記切り込み済み複層貼着体の加飾フィルム部材及び粘着層のうち上記切り込み済み対応部位の内側部位を保護フィルムと共に一体的に除去する第7工程(S7)とを備えて、
上記第1〜第7の工程を上記所定の雰囲気温度の環境内で行い、上記第7工程後所定の短時間内に化粧シートの異常或いは粘着層と遊技基板との間に異物の混入が発見されたとき、化粧シートを遊技基板から剥がして新たな化粧シートを遊技基板に上記第1〜第7の工程を経て貼着し直すことで製造するようにしたことを特徴とする。
Moreover, according to the description of claim 13, the present invention provides
In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As a game board, a game board (10) made of a transparent polycarbonate resin or a transparent acrylic resin formed so as to have an opening (11) required for assembling an effect display device among various game parts is prepared in advance. And
A protective film roll (50) made of a first thermoplastic resin longitudinal film body and a decorative film member roll (40) made of a transparent second thermoplastic resin longitudinal film body are prepared in advance,
In addition, a transparent adhesive that exhibits an adhesive property that is low immediately after the attachment when it is attached to the surface of the game board and that increases with the passage of time in an environment of a predetermined atmosphere temperature and the adhesive material. Adhesive material layer (81) to be adhered, along with one side surface of the adhesive material layer, a longitudinal one-side separation layer (82) made of polyester resin, and adhered along the other side surface of the adhesive material layer Prepare in advance an adhesive material roll (80) formed with the longitudinal other side separation layer (83) made of polyester resin,
A first step (S1) for forming a film adhering roll body by adhering a protective film roll along a decorative film member roll;
A second step (S2) of forming the film sticking roll as a sticking film layer (60a) comprising a protective film (21) and a decorative film member (20) by cutting the film sticking roll body at a length corresponding to the game board; ,
A transparent first special pattern for forming a predetermined pattern (22) on the printed surface of the sticking film layer opposite to the protective film of the decorative film member and attaching the hologram foil to a part of the printed surface. The ink (24) is printed, and the hologram foil (25) is transferred to the printed portion of the first special ink. Further, between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred. In order to fill the level difference and flatten the surface, a second transparent special ink (26) is poured into a portion where the hologram foil is not transferred to form a printed adhesive film layer (71). 3 steps,
While peeling off the one side separation layer from the adhesive material roll, the adhesive material layer of the adhesive material roll is adhered along the printing side of the decorative film member of the printing adhesive film layer, and is aligned with the printing adhesive film layer. A fourth step (S4) to form as a multi-layer adhesive body (100) comprising a protective film, a decorative film member, an adhesive layer and another side separation layer;
5th process (S5) which cut | disconnects the site | part corresponding with respect to the internal peripheral surface of the said opening part of a game board among multi-layer stickers from the other side separated layer to a decoration film member except a protective film (S5). )When,
The above-mentioned cut protective film, decorative film member, pressure-sensitive adhesive layer and other-side separation layer, the cut multilayer adhesive body (100a), while peeling the other-side separation layer, the adhesive layer, And a sixth step (S6) for sticking with pressing with a pressure within a predetermined pressure range;
After the sixth step, while peeling off the protective film from the decorative film member, the inner portion of the cut corresponding portion of the decorative film member and the adhesive layer of the cut multilayered adhesive body is integrated with the protective film. A seventh step (S7) to be removed,
The first to seventh steps are carried out in the environment of the predetermined atmospheric temperature, and an abnormality of the decorative sheet or a foreign matter mixed between the adhesive layer and the game board is found within a predetermined short time after the seventh step. When this is done, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the above first to seventh steps to manufacture the decorative sheet.
これにより、請求項7に記載の発明と実質的に同様な作用効果を達成し得る。 Thereby, the effect substantially the same as that of the invention of Claim 7 can be achieved.
また、本発明は、請求項14の記載によれば、請求項13に記載の遊技盤の製造方法において、
上記第3工程では、転写面に糊が付いているホログラム箔を転写させる場合には、上記所定の図柄の形成後、上記透明な第1特殊インクの印刷前に、当該印刷面全体に亘って、ホログラム箔の定着を防止するための透明な第3特殊インクを印刷することを特徴とする。
According to the description of claim 14, the present invention provides a game board manufacturing method according to claim 13,
In the third step, when transferring the hologram foil with glue on the transfer surface, after the predetermined pattern is formed and before the transparent first special ink is printed, the entire print surface is covered. A transparent third special ink for preventing the fixing of the hologram foil is printed.
これにより、請求項5に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that attained by the 5th aspect can be attained.
また、本発明は、請求項15の記載によれば、請求項13または14に記載の遊技盤の製造方法において、
上前記第3工程では、上記第1特殊インクを印刷するときには、ホログラム箔の転写を安定させるために、当該加飾フィルム部材の外周に沿って帯状の領域(24a)を印刷し、
上記第5工程では、当該切り込みと併せて、ホログラム箔が転写された上記帯状の領域を含む領域を当該加飾フィルム部材から切断して、上記切り込み済み複層貼着体の外周面形状を遊技基板の外周面形状に合わせることを特徴とする。
According to a fifteenth aspect of the present invention, in the game board manufacturing method according to the thirteenth or fourteenth aspect,
In the third step, when printing the first special ink, in order to stabilize the transfer of the hologram foil, a band-shaped region (24a) is printed along the outer periphery of the decorative film member,
In the fifth step, in addition to the cut, a region including the band-shaped region to which the hologram foil has been transferred is cut from the decorative film member, and the outer peripheral surface shape of the cut multilayer adhesive body is played. It is characterized by conforming to the shape of the outer peripheral surface of the substrate.
これにより、請求項6に記載の発明と実質的に同様の作用効果を達成し得る。 Thereby, substantially the same effect as that of the sixth aspect of the invention can be achieved.
また、本発明は、請求項16の記載のように、請求項6〜15のいずれか1つに記載の遊技盤の製造方法において、第1或いは第2の熱可塑性樹脂は、ポリエチレンテレフタレートであることを特徴とするようにしてもよい。 According to the present invention, as described in claim 16, in the game board manufacturing method according to any one of claims 6 to 15, the first or second thermoplastic resin is polyethylene terephthalate. You may make it feature.
なお、上記各手段の括弧内の符号は、後述する実施形態に記載の具体的手段との対応関係を示す。 In addition, the code | symbol in the bracket | parenthesis of each said means shows a corresponding relationship with the specific means as described in embodiment mentioned later.
以下、本発明の一実施形態を図面により説明する。 Hereinafter, an embodiment of the present invention will be described with reference to the drawings.
図1は、本発明を適用してなるパチンコ遊技機を示している。当該遊技盤(以下、遊技盤Bという)は、図1及び図2にて示すごとく、遊技基板10及び化粧シートSを備えている。本実施形態において、化粧シートSは、その裏面にて、後述するごとく、遊技基板10の表面に貼着されるものである。また、種々の遊技部品(図示しない)が遊技基板10の裏面に或いは化粧シートSを介し遊技基板10の表面に組み付けられる。なお、化粧シートSの表面は、遊技盤Bの盤面を構成する。
FIG. 1 shows a pachinko gaming machine to which the present invention is applied. The game board (hereinafter referred to as game board B) includes a
遊技基板10は、ポリカーボネート樹脂(以下、PC樹脂ともいう)でもって、平板状に形成されているもので、この遊技基板10には、中央開口部11が、上記種々の遊技部品のうちの演出表示装置(図示しない)を一盤面部品として組み付けるために形成されている。なお、上記演出表示装置は、当該パチンコ遊技機による遊技に伴い、種々の演出表示を行うものである。また、上記PC樹脂は、熱可塑性樹脂のうちのポリエステルの一種であって、高い剛性を有するとともに、無色透明である。
The
本実施形態において、遊技基板10の面外形形状は、図1或いは図2から分かるように、幅W×長さLからなる矩形形状となっている。
In the present embodiment, the outer surface shape of the
化粧シートSは、図1或いは図2にて示すごとく、加飾フィルム部材20と、粘着層30とによって構成されている。加飾フィルム部材20は、ポリエステルの一種である無色透明のポリエチレンテレフタレート(以下、PETともいう)でもって、所定の厚さ範囲以内の厚さにて、遊技基板10の面外形形状と同一の面外形形状を有するように形成されている。このことは、加飾フィルム部材20が、その表面にて、遊技基板10の面外形形状と同一の面外形形状を有することを意味する。また、上記所定の厚さ範囲は、例えば、75(μm)〜188(μm)の範囲をいう。ここで、厚さの下限を75(μm)としたのは、75(μm)未満では、薄すぎて破れ易く取り扱いに不便を感ずるためである。厚さの上限を188(μm)としたのは、当該188(μm)を超えて厚くなると、遊技釘の打ち込み時に加飾フィルム部材20が遊技基板10から浮いてしまうためである。本実施形態では、加飾フィルム部材20として、100(μm)の厚さのものを用いている。
As shown in FIG. 1 or FIG. 2, the decorative sheet S includes a
なお加飾フィルム部材20には、中央開口部20aが、遊技基板10の中央開口部11に対応するように形成されている(図1或いは図2参照)。
The
粘着層30は、所定の粘着剤でもって、所定の厚さ範囲以内の厚さ(例えば、50(μm))にて、遊技基板10の面外形形状と同一の面外形形状を有するように層状に形成されている。本実施形態において、上記所定の厚さ範囲は、25(μm)〜70(μm)である。
The
ここで、当該所定の厚さ範囲の下限を25(μm)としたのは、粘着層30が25(μm)よりも薄すぎると、破れ易く取り扱いにも不便であるのは勿論のこと、粘着層30の遊技基板10に対する定着が甘く、遊技釘の打ち込み時の衝撃に耐えられないためである。また、当該所定の厚さ範囲の上限を70(μm)としたのは、粘着層30が70(μm)よりも厚すぎると、柔軟性に欠け取り扱いにも不便であるためである。なお、上記所定の厚さ範囲は、より好ましくは、40(μm)〜50(μm)としてもよい。
Here, the lower limit of the predetermined thickness range is set to 25 (μm). If the
しかして、当該粘着層30は、その表面にて、後述のごとく、加飾フィルム部材20の裏面に貼着されており、この粘着層30は、その裏面にて、後述のごとく、遊技基板10の表面に貼着されている(図1参照)。なお、粘着層30には、中央開口部30a(図1参照)が遊技基板10の中央開口部11に対応して形成されているが、当該中央開口部30aは、図2では、便宜上、省略されている。
Therefore, the
本実施形態において、上記所定の粘着剤としては、日栄化工株式会社製のWF−D804型アクリル系粘着剤が採用されており、このWF−D804型アクリル系粘着剤は、所定の粘着力特性を有する。 In the present embodiment, a WF-D804 type acrylic pressure sensitive adhesive made by Nichiei Kako Co., Ltd. is adopted as the predetermined pressure sensitive adhesive, and the WF-D804 type acrylic pressure sensitive adhesive has a predetermined adhesive property. Have.
ここで、当該アクリル系粘着剤の粘着力特性を雰囲気温度との関係において測定してみた。測定方法は次の通りである。 Here, the adhesive strength characteristic of the acrylic adhesive was measured in relation to the ambient temperature. The measuring method is as follows.
WF−D804型アクリル系粘着剤からなる粘着層の剥離面を25(μm)の厚さのPETで裏打ちした後25(mm)×150(mm)の大きさに切断して粘着試料として複数準備する。このように準備した各粘着試料を、複数の所定の雰囲気温度の各々の環境において互いに異なる4種類の被着体の各々に貼り合わせてそれぞれ貼り合わせ試料とする。 A peeled surface of an adhesive layer made of WF-D804 acrylic adhesive is lined with PET having a thickness of 25 (μm) and then cut into a size of 25 (mm) × 150 (mm) to prepare a plurality of adhesive samples. To do. Each of the prepared adhesive samples is bonded to each of four different adherends in each environment at a plurality of predetermined atmospheric temperatures to obtain a bonded sample.
ここで、上述の所定の雰囲気温度は、0(℃)、10(℃)及び常温(20(℃))とする。従って、上述した互いに異なる被着体毎に、粘着試料を3つずつ準備する。また、上述の4種類の被着体は、例えば、ステンレス鋼(厚さ360(mm)で研磨済み)からなるシート(以下、ステンレスシートともいう)、ポリカーボネート樹脂からなるシート(以下、PCシートともいう)、アクリル樹脂からなるシート(以下、アクリルシートともいう)及びPETならなるシート(以下、PETシートともいう)をいう。なお、上記各貼り合わせ試料のうち、ステンレスシート、PCシート、アクリルシート及びPETシートをそれぞれ貼り合わせた各試料を、それぞれ、ステンレス試料、PC試料、アクリル試料及びPET試料ともいう。 Here, the predetermined atmospheric temperature is 0 (° C.), 10 (° C.), and normal temperature (20 (° C.)). Therefore, three adhesion samples are prepared for each of the different adherends described above. The four types of adherends described above include, for example, a sheet (hereinafter also referred to as a stainless sheet) made of stainless steel (previously polished with a thickness of 360 (mm)) and a sheet (hereinafter also referred to as a PC sheet) made of polycarbonate resin. A sheet made of acrylic resin (hereinafter also referred to as an acrylic sheet) and a sheet made of PET (hereinafter also referred to as a PET sheet). In addition, each sample which bonded the stainless steel sheet, PC sheet | seat, an acrylic sheet, and a PET sheet among said each bonding sample is also called a stainless steel sample, a PC sample, an acrylic sample, and a PET sample, respectively.
しかして、貼り合わせ試料毎に、当該貼り合わせ試料を、2(kg)のゴムローラでもって、一往復により、所定の基台上において圧着する。その後、当該各貼り合わせ試料を、引っ張り試験機でもって、引っ張り試験を施して粘着力を測定する。なお、このような貼り合わせ試料毎の上記ゴムローラによる圧着及び引っ張り試験機による引っ張り試験は、上述した貼り合わせ試料毎の雰囲気温度の環境において、上述のゴムローラによる圧着後、20(分)の経過時及び24(時間)の経過時間の経過時に行う。但し、剥離条件は、剥離角度180°及び剥離速度300(mm/分)とする。 Thus, for each bonded sample, the bonded sample is pressed on a predetermined base by one reciprocation with a 2 (kg) rubber roller. Thereafter, each of the bonded samples is subjected to a tensile test with a tensile tester and the adhesive strength is measured. It should be noted that the pressure bonding with the rubber roller for each bonded sample and the tensile test with the tensile tester are performed at the time of 20 (minutes) after the pressure bonding with the rubber roller in the above-described atmosphere temperature environment for each bonded sample. And 24 (hours) elapsed. However, the peeling conditions are a peeling angle of 180 ° and a peeling speed of 300 (mm / min).
上記試験結果は、次の表1の通りである。 The test results are as shown in Table 1 below.
この表1において、試験項目である粘着力は、ステンレス試料、PC試料、アクリル試料及びPET試料の各々の粘着力をいい、当該各粘着力は、ステンレス試料、PC試料、アクリル試料及びPET試料の各々においてステンレスシート、PCシート、アクリルシート及びPETシートの上記所定の基台からの剥離強度に対応する。経過時間は、ステンレスシート、PCシート、アクリルシート或いはPETシートの上記所定の基台に対する貼着時からの経過時間をいう。また、雰囲気温度0(℃)、10(℃)及び20(℃)は、それぞれ、ステンレス試料、PC試料、アクリル試料及びPET試料の作成及び粘着力の測定を行う雰囲気温度をいう。 In Table 1, the test item adhesive strength refers to the adhesive strength of each of the stainless steel sample, the PC sample, the acrylic sample, and the PET sample, and the adhesive strength of each of the stainless steel sample, the PC sample, the acrylic sample, and the PET sample. Each corresponds to the peel strength of the stainless steel sheet, PC sheet, acrylic sheet and PET sheet from the predetermined base. The elapsed time refers to the elapsed time from the time when the stainless sheet, PC sheet, acrylic sheet or PET sheet is attached to the predetermined base. Moreover, atmospheric temperature 0 (degreeC), 10 (degreeC), and 20 (degreeC) means the atmospheric temperature which produces stainless steel sample, PC sample, an acrylic sample, and a PET sample, and measures an adhesive force, respectively.
しかして、表1によれば、ステンレス試料の粘着力は、20(分)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、2.2(N/25mm)、4.3(N/25mm)及び15.4(N/25mm)であった。 Thus, according to Table 1, the adhesive strength of the stainless steel sample was 20 (minutes), and the ambient temperature was 0 (° C), 10 (° C), and 20 (° C), respectively. 2.2 (N / 25 mm), 4.3 (N / 25 mm) and 15.4 (N / 25 mm).
これによれば、当該ステンレス試料の粘着力は、20(分)の経過時には、雰囲気温度0(℃)及び10(℃)にて、2.2(N/25mm)、4.3(N/25mm)と非常に低く、雰囲気温度20(℃)では、15.4(N/25mm)と高い値となっている。 According to this, the adhesive strength of the stainless steel sample was 2.2 (N / 25 mm), 4.3 (N / N) at an atmospheric temperature of 0 (° C.) and 10 (° C.) when 20 minutes passed. 25 mm), which is as low as 15.4 (N / 25 mm) at an atmospheric temperature of 20 (° C.).
また、当該ステンレス試料の粘着力は、24(時間)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、23.1(N/25mm)、23.2(N/25mm)及び24.2(N/25mm)であった。 Further, the adhesive strength of the stainless steel sample was 23.1 (N / s) under each environment of 0 (° C.), 10 (° C.), and 20 (° C.) at the elapse of 24 (hours). 25 mm), 23.2 (N / 25 mm) and 24.2 (N / 25 mm).
これによれば、当該ステンレス試料の粘着力は、24(時間)の経過時には、雰囲気温度0(℃)、10(℃)及び20(℃)のいずれにても、相互に殆ど変らないものの、経過時間20(分)の場合に比べ、非常に高い値或いはかなり高い値となっている。 According to this, although the adhesive strength of the stainless steel sample is 24 (hours), the atmospheric temperature is hardly changed at any of 0 (° C.), 10 (° C.) and 20 (° C.), Compared with the elapsed time of 20 (minutes), the value is very high or considerably high.
また、PC試料の粘着力は、20(分)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、2.7(N/25mm)、15.0(N/25mm)及び16.7(N/25mm)であった。 Further, the adhesive strength of the PC sample was 2.7 (N / 25 mm) at the time of 20 (minutes) under each environment of atmospheric temperature 0 (° C.), 10 (° C.) and 20 (° C.). ) 15.0 (N / 25 mm) and 16.7 (N / 25 mm).
これによれば、当該PC試料の粘着力は、20(分)の経過時には、雰囲気温度0(℃)において、ステンレス試料の場合と同様に非常に低く、雰囲気温度10(℃)において、ステンレス試料の場合よりも非常に高く、また、雰囲気温度20(℃)において、ステンレス試料の場合と殆ど変らない。 According to this, the adhesive strength of the PC sample is very low at the atmospheric temperature of 0 (° C.) as in the case of the stainless steel sample at the time of 20 (minutes), and the stainless steel sample at the atmospheric temperature of 10 (° C.). It is much higher than in the case of the above, and is almost the same as the case of the stainless steel sample at the atmospheric temperature of 20 (° C.).
また、当該PC試料の粘着力は、24(時間)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、22.3(N/25mm)、22.5(N/25mm)及び23.4(N/25mm)であった。 Moreover, the adhesive strength of the PC sample was 22.3 (N / s) under the respective environments of ambient temperatures of 0 (° C.), 10 (° C.), and 20 (° C.) after 24 hours. 25mm), 22.5 (N / 25mm) and 23.4 (N / 25mm).
これによれば、当該PC試料の粘着力は、24(時間)の経過時には、雰囲気温度0(℃)、10(℃)及び20(℃)のいずれにても、相互に殆ど変らないものの、ステンレス試料の場合とほぼ同様に高い値となっている。 According to this, although the adhesive strength of the PC sample is 24 (hours), it hardly changes each other at any of atmospheric temperatures 0 (° C.), 10 (° C.) and 20 (° C.), The value is almost the same as in the case of the stainless steel sample.
また、アクリル試料の粘着力は、20(分)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、2.8(N/25mm)、14.0(N/25mm)及び15.7(N/25mm)であった。 Further, the adhesive strength of the acrylic sample was 2.8 (N / 25 mm) in each environment at an ambient temperature of 0 (° C.), 10 (° C.), and 20 (° C.) when 20 (minutes) passed. ), 14.0 (N / 25 mm) and 15.7 (N / 25 mm).
これによれば、当該アクリル試料の粘着力は、20(分)の経過時には、雰囲気温度0(℃)において、ステンレス試料及びPC試料の双方の場合と同様に非常に低く、雰囲気温度10(℃)及び20(℃)において、PC試料の場合と殆ど変らないが、10(℃)では、ステンレス試料の場合よりもかなり高くなっている。 According to this, the adhesive strength of the acrylic sample is very low at the time of 20 (minutes) at the atmospheric temperature 0 (° C.) as in the case of both the stainless steel sample and the PC sample, and the atmospheric temperature 10 (° C. ) And 20 (° C.) are almost the same as those of the PC sample, but at 10 (° C.), it is considerably higher than that of the stainless steel sample.
また、当該アクリル試料の粘着力は、24(時間)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、18.9(N/25mm)、19.6(N/25mm)及び19.8(N/25mm)であった。 In addition, the adhesive strength of the acrylic sample was 18.9 (N / hour) under each environment of ambient temperatures of 0 (° C.), 10 (° C.), and 20 (° C.) after 24 hours. 25 mm), 19.6 (N / 25 mm) and 19.8 (N / 25 mm).
これによれば、当該アクリル試料の粘着力は、24(時間)の経過時には、雰囲気温度0(℃)、10(℃)及び20(℃)のいずれにても、相互に殆ど変らないが、ステンレス試料の場合よりも幾分低いものの、ほぼ同様に高い値となっている。 According to this, the adhesive strength of the acrylic sample hardly changes each other at any of the atmospheric temperatures 0 (° C.), 10 (° C.) and 20 (° C.) when 24 (hours) elapses. Although it is somewhat lower than that of the stainless steel sample, the value is almost the same.
また、PET試料の粘着力は、20(分)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、1.8(N/25mm)、5.0(N/25mm)及び14.6(N/25mm)であった。 Further, the adhesive strength of the PET sample was 1.8 (N / 25 mm) at the time of 20 (minutes) under each of the ambient temperatures of 0 (° C.), 10 (° C.), and 20 (° C.). ), 5.0 (N / 25 mm) and 14.6 (N / 25 mm).
これによれば、当該PET試料の粘着力は、20(分)の経過時には、雰囲気温度0(℃)では、ステンレス試料、PC試料及びアクリル試料の場合と殆ど変らず、非常に低く、雰囲気温度10(℃)では、ステンレス試料の場合と同様に非常に低く、また、雰囲気温度20(℃)では、ステンレス試料、PC試料及びアクリル試料の場合と殆ど変らない。 According to this, the adhesive strength of the PET sample is very low at the atmospheric temperature of 0 (° C.) when 20 (minutes) has passed, and is very low at the atmospheric temperature. At 10 (° C.), it is very low as in the case of the stainless steel sample, and at an atmospheric temperature of 20 (° C.), it is almost the same as in the case of the stainless steel sample, PC sample, and acrylic sample.
また、当該PET試料の粘着力は、24(時間)の経過時にて、雰囲気温度0(℃)、10(℃)及び20(℃)の各環境のもと、それぞれ、16.2(N/25mm)、16.5(N/25mm)及び16.9(N/25mm)であった。 In addition, the adhesive strength of the PET sample was 16.2 (N / C) under each environment of ambient temperature 0 (° C.), 10 (° C.), and 20 (° C.) after 24 hours. 25 mm), 16.5 (N / 25 mm) and 16.9 (N / 25 mm).
これによれば、当該PET試料の粘着力は、24(時間)の経過時には、雰囲気温度0(℃)、10(℃)及び20(℃)のいずれにても、相互に殆ど変らないが、アクリル試料の場合よりも幾分低いものの、ほぼ同様に高い値となっている。 According to this, the adhesive strength of the PET sample hardly changes each other at any of the atmospheric temperatures 0 (° C.), 10 (° C.) and 20 (° C.) when 24 (hours) have passed. Although it is somewhat lower than that of the acrylic sample, the value is almost the same.
以上によれば、ステンレス試料、PC試料、アクリル試料及びPET試料は、それぞれ、固有の粘着力特性を有するものの、各々の粘着力は、時間の経過に伴い高くなる傾向を有するものの、ステンレスシート、PCシート、アクリルシート或いはPETシートの上記所定の基台に対する貼り合わせ直後において高くなることはない。換言すれば、WF−D804型アクリル系粘着剤の粘着力特性は、上記貼り合わせ直後には非常に低く時間の経過に伴い緩やかに高くなる傾向を有する。 According to the above, although the stainless steel sample, the PC sample, the acrylic sample, and the PET sample each have unique adhesive strength characteristics, each adhesive strength tends to increase with time, but the stainless steel sheet, It does not increase immediately after the PC sheet, acrylic sheet or PET sheet is bonded to the predetermined base. In other words, the adhesive strength characteristics of the WF-D804 acrylic adhesive are very low immediately after the bonding, and tend to increase gradually with the passage of time.
本実施形態においては、ステンレスシート、PCシート、アクリルシート或いはPETシートの上記所定の基台に対する貼着時の直後(後述する所定の短時間以内、例えば、貼着後少なくとも20(分)以内)の粘着力は、雰囲気温度0(℃)、10(℃)及び20(℃)のいずれであっても、ステンレスシート、PCシート、アクリルシート或いはPETシートを上記所定の基台から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力であると認められる。 In the present embodiment, immediately after adhering a stainless steel sheet, PC sheet, acrylic sheet or PET sheet to the predetermined base (within a predetermined short time described later, for example, within at least 20 (minutes) after adhering). The adhesive strength of the stainless steel sheet, PC sheet, acrylic sheet or PET sheet leaves a trace from the predetermined base at any of atmospheric temperatures 0 (° C), 10 (° C) and 20 (° C). It is recognized that the adhesive strength is low enough that it can be removed cleanly and easily.
例えば、PCシートでは、上記粘着力は、16.7(N/25mm)程度であれば、上述した基台から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力に相当する。また、上記アクリルシートでは、上記粘着力は、15.7(N/25mm)程度であれば、上述した基台から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力に相当する。 For example, in the case of a PC sheet, if the adhesive strength is about 16.7 (N / 25 mm), it corresponds to an adhesive strength that is low enough to be easily and easily peeled off without leaving a trace from the above-mentioned base. Moreover, in the said acrylic sheet, if the said adhesive force is about 15.7 (N / 25mm), it is corresponded to low adhesive force to such an extent that it can peel off neatly without leaving a trace from the base mentioned above.
また、上記粘着力が、ステンレスシート、PCシート、アクリルシート或いはPETシートを上記所定の基台から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力であれば、上述した貼着後少なくとも20(分)以内に限ることなく、20(分)を、例えば5(分)程度、超えてもよい。なお、20(分)未満であれば、上述した低い粘着力という条件を満たすことは容易に理解できる。 If the adhesive strength is low enough that the stainless steel sheet, PC sheet, acrylic sheet or PET sheet can be removed cleanly and easily without leaving a trace from the predetermined base, after the above-mentioned pasting Without being limited to at least 20 (minutes), 20 (minutes) may be exceeded by, for example, about 5 (minutes). In addition, if it is less than 20 (minutes), it can be easily understood that the above-described condition of low adhesive strength is satisfied.
また、上述した雰囲気温度の範囲は、0(℃)、10(℃)及び20(℃)に限ることなく、0(℃)〜20(℃)の範囲以内であってもよく、また、20(℃)よりも高くても、上記粘着力が、上述した貼着時の直後において、ステンレスシート、PCシート、アクリルシート或いはPETシートを上記所定の基台から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低く、かつ、上記貼着時の後、例えば、24(時間)経過した時点において、良好な値を確保し得る温度の範囲であればよいことは確認済みである。 The range of the atmospheric temperature described above is not limited to 0 (° C.), 10 (° C.), and 20 (° C.), and may be within the range of 0 (° C.) to 20 (° C.). Even if it is higher than (° C.), the adhesive strength is clean and easy without leaving a trace from the predetermined base on the stainless sheet, PC sheet, acrylic sheet or PET sheet immediately after the above-mentioned sticking. It has been confirmed that the temperature may be within a temperature range that can ensure a good value when it is low enough to be peeled off and, for example, 24 (hours) after the sticking.
換言すれば、本実施形態における遊技基板10の形成材料は、上述のごとく、PC樹脂であることから、上述のPC試料の粘着力特性と同様の粘着力特性を有する。従って、遊技基板10と化粧シートSとの貼り合わせ直後の粘着力は、化粧シートSを遊技基板10から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力であると認められる。なお、この点については、実際に、化粧シートSを遊技基板10から剥がしてみることで、化粧シートSを遊技基板10から痕跡を残すことなくきれいにかつ容易に剥がし得ることは確認済みである。
In other words, since the forming material of the
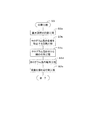
次に、以上のように構成した本実施形態の遊技盤Bの製造方法について図3を参照して説明する。保護フィルムロール貼着工程S1においては、まず、加飾フィルムロール40及び保護フィルムロール50を準備する(図5参照)。なお、当該保護フィルムロール貼着工程S1から保護フィルム剥がし工程S7までの処理は、10(℃)の雰囲気温度の環境にてなされる。
Next, a manufacturing method of the game board B of the present embodiment configured as described above will be described with reference to FIG. In the protective film roll sticking step S1, first, a
ここで、加飾フィルムロール40は、複数の加飾フィルム部材20として切断形成する前のPET製長手状フィルム体を加飾フィルム部材用フィルム体としてロール状に巻いたものである。また、保護フィルムロール50は、後述のごとく加飾フィルム部材20を保護する保護フィルム21(図20参照)を複数切断形成する前の他のPET製長手状フィルム体を保護フィルム用フィルム体としてロール状に巻いたものである。なお、加飾フィルムロール40は、上述した加飾フィルム部材20と同様の厚さを有する。また、保護フィルムロール50は、50(μm)の厚さを有する。ここで、50(μm)の厚さとしたのは、これより薄いと、カールが発生して加飾フィルムロール40との貼着を良好に行うことができないためである。
Here, the
しかして、このように準備した保護フィルムロール50を、図5にて示すごとく、加飾フィルムロール40上にその長手方向に沿い貼着して、フィルム貼着ロール体60(図6参照)として形成する。なお、保護フィルムロール50は、その裏面にて、加飾フィルムロール40の表面に貼着される。
And as shown in FIG. 5, the
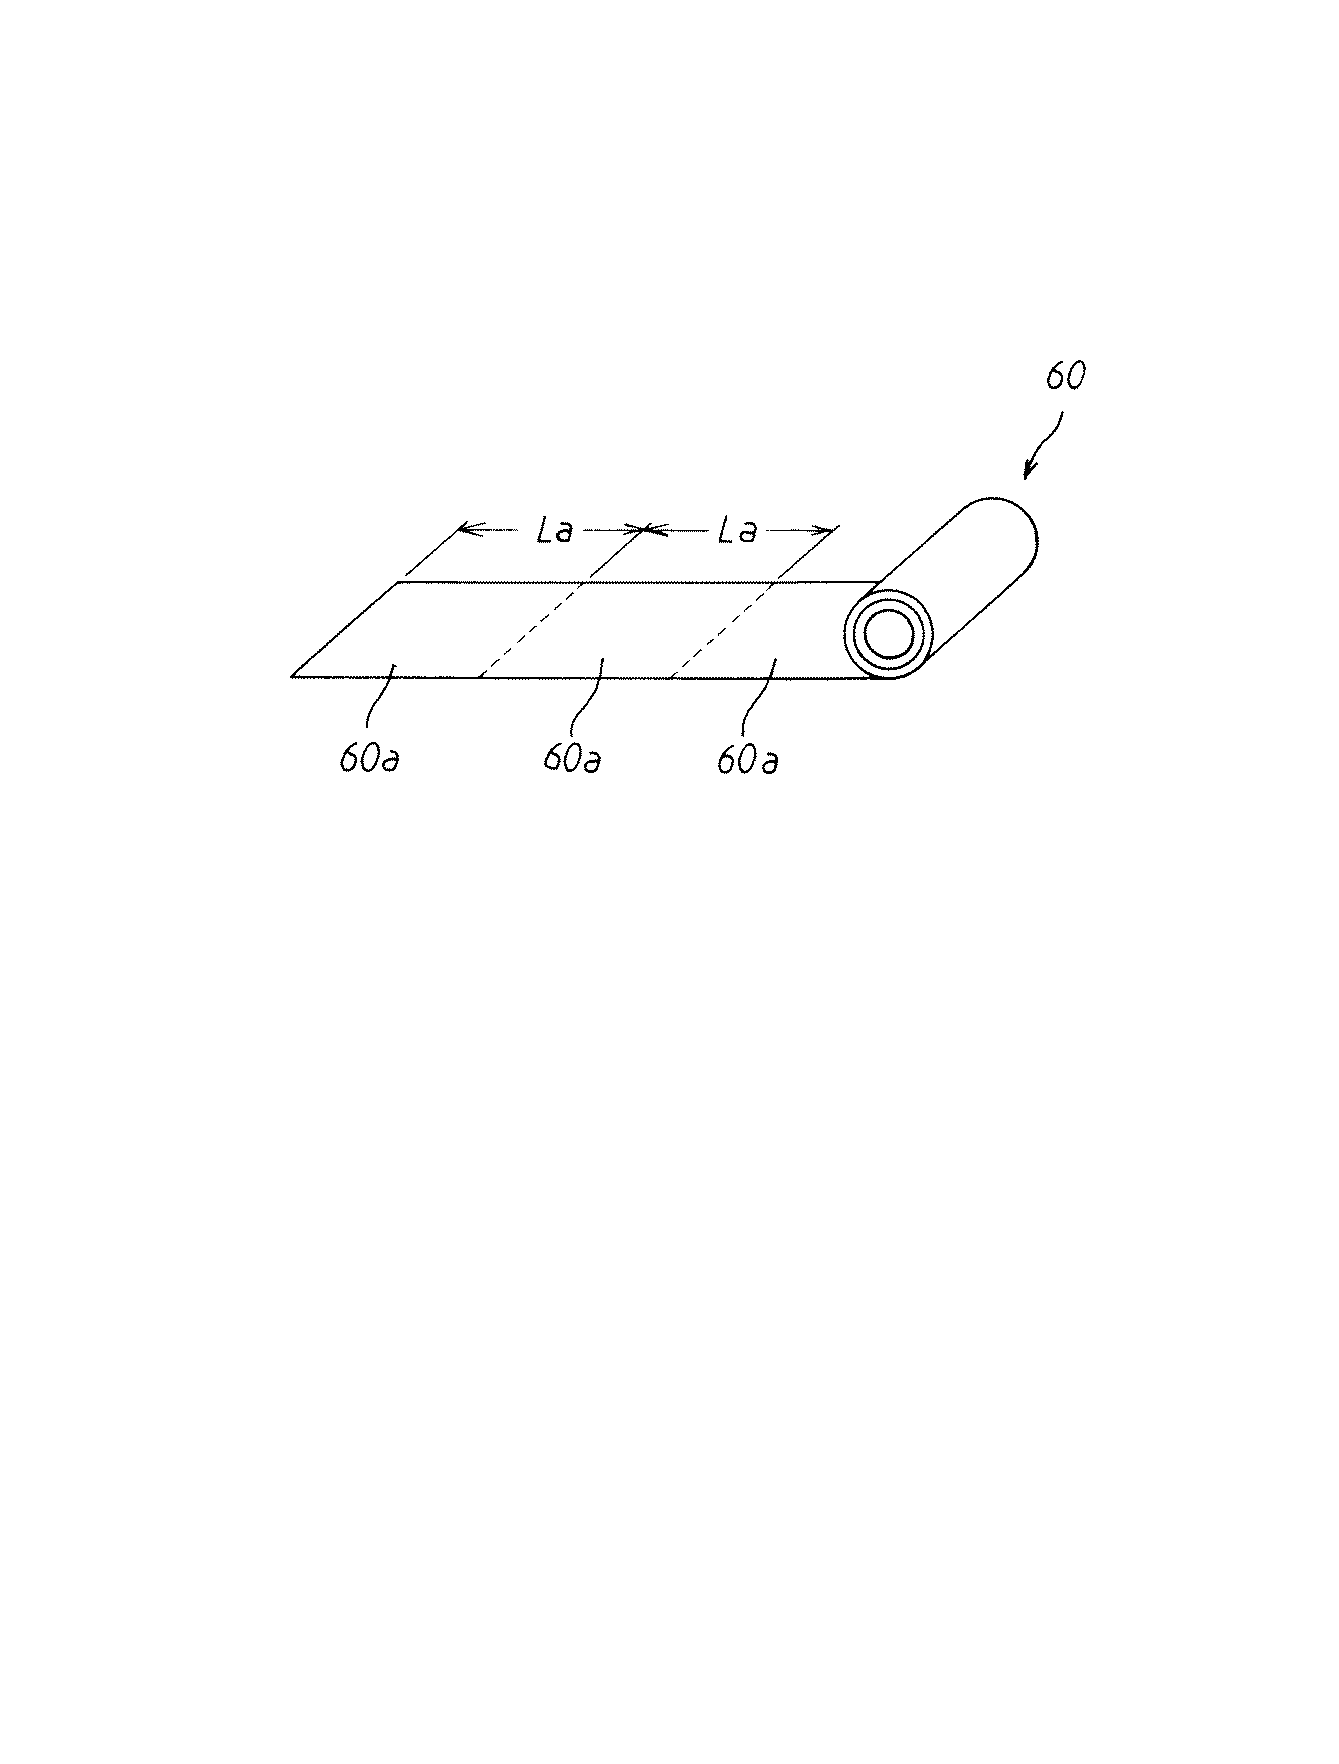
然る後、切断工程S2において、フィルム貼着ロール体60を、図6にて破線により示すごとく、順次、所定の切断間隔にて切断して、貼着フィルム層60a(図6及び図7参照)として形成する。本実施形態では、上述の所定の切断間隔は、遊技基板10の長さLより若干長いLaである。このように切断間隔を遊技基板10の長さLより長く設定したのは、後述する切り込み工程S5の処理において、貼着フィルム層60aの外周面形状は、これに包含される化粧シートSの外周面形状に切断されるからである(図23参照)。
Thereafter, in the cutting step S2, as shown by a broken line in FIG. 6, the film sticking
また、貼着フィルム層60aは、保護フィルム21及び加飾フィルム部材20を貼着した構成となり、保護フィルム21は、その裏面にて、加飾フィルム部材20の表面に貼着されている(図7参照)。
Moreover, the sticking
このように複数の貼着フィルム層60aが切断形成されると、次の印刷工程S3において、貼着フィルム層60aの裏面、即ち、加飾フィルム部材20の裏面に、所定の模様、図柄等の印刷パターンを印刷し、さらにそれに重ねて所定の位置にホログラム箔を転写する。ホログラム箔は通常、単一の光彩を放つ金属箔の表面に、レーザー光線の光の干渉現象を利用して立体的な輝きを表現する技術を要した特殊箔の一つである。本願発明では、従来の加飾、即ち、上記印刷パターンによる加飾にはない、新しい加飾をホログラム箔により行うようにしている。
When the plurality of adhesive film layers 60a are cut and formed in this way, in the next printing step S3, a predetermined pattern, design, or the like is formed on the back surface of the
印刷工程S3は、図4にて示すごとく、複数の工程S3a〜S3eによって構成されている。まず工程S3aにおいて、オフセット印刷にて基本図柄を印刷する。 As shown in FIG. 4, the printing process S <b> 3 includes a plurality of processes S <b> 3 a to S <b> 3 e. First, in step S3a, a basic symbol is printed by offset printing.
オフセット印刷は、本実施形態では、CMYK(シアン、マゼンタ、イエロー、ブラック)の各色インクを用いてカラーでなされる。具体的には図8にて示すごとく、ベルトコンベア200上に加飾フィルム部材20を、その裏面を上向きにして置く。そして、ベルトコンベア200が当該加飾フィルム部材20を図8にて図示右方向に搬送するに従い、当該加飾フィルム部材20は上記各色インクで印刷する各色印刷機210〜213を通るので、所望の基本図柄が所望の色でオフセット印刷される。図9は、オフセット印刷された結果、加飾フィルム部材20(の裏面)上にオフセットインク22が載った状態の一例を示す断面図である。
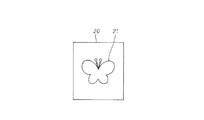
本実施形態では、図17に示すごとく、基本図柄として「蝶」が印刷されているが、図9は、加飾フィルム部材20上にオフセット印刷された状態を便宜的に表すものであって、図17の印刷結果と正確に対応しているものではない。オフセットインク22の厚さは、4(μm)程度である。
In this embodiment, offset printing is performed in color using each color ink of CMYK (cyan, magenta, yellow, black). Specifically, as shown in FIG. 8, the
In this embodiment, as shown in FIG. 17, “butterfly” is printed as a basic design, but FIG. 9 represents the state of offset printing on the
なお上記工程S3aでは、加飾フィルム部材20上に基本図柄を形成する際に、4色のインクにて行うようにしたが、色数はこれより多くても少なくてもよい。また、印刷手法も、オフセット印刷に限らず、シルク印刷であってもよい。さらに、印刷手法ではなく他の手法、例えば、ホットスタンプやフィルム貼り合わせなどを用いてもよい。
In the step S3a, when the basic symbol is formed on the
次に工程S3bにおいて、オフセット印刷にて、ホログラム箔の定着を防止するインクを印刷する。このインクとして、本実施形態では、透明なUV系特殊インク(樹脂)を用いている。そして印刷は、図10に示すごとく、加飾フィルム部材20全体に行われる。このUV系特殊インク23の厚さは、1(μm)程度であるが、それはオフセットインク22からの厚みであり、オフセットインク22が載っていない加飾フィルム部材20の表面からは5(μm)程度である。なお、UV系特殊インク23は、ホログラム箔側に転写用の糊が付いている場合に、ホログラム箔がその転写時、転写すべきでない部分に転写されるのを防ぐためのものである。従って、ホログラム箔として転写用の糊が付いていないものを用いる場合には、この工程S3bを省略することができる。
Next, in step S3b, ink for preventing fixing of the hologram foil is printed by offset printing. In this embodiment, a transparent UV special ink (resin) is used as this ink. And printing is performed to the whole
次に工程S3cにおいて、シルク印刷にて、ホログラム箔を付着させるインク(糊)を印刷する。このインクとして、本実施形態では、透明なUV硬化型インク(樹脂)を用いている。 Next, in step S3c, ink (glue) to which the hologram foil is attached is printed by silk printing. In this embodiment, a transparent UV curable ink (resin) is used as this ink.
シルク印刷は、図11或いは図12に示すごとく、シルクスクリーン版230に形成したオープニング231からスキージ240を用いてインク24を押し出して、印刷パターンを印刷するものである。この印刷も、ローラコンベア220を用いて、加飾フィルム部材20を図11にて図示左方向に搬送して行っている。
As shown in FIG. 11 or FIG. 12, the silk printing is to print a printing pattern by extruding the
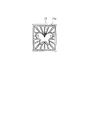
ホログラム箔は、後述する図19に示すごとく、基本図柄(本実施形態では、上記図17の「蝶」)上或いはその周囲の一部に転写されるので、UV硬化型インク24は、図18に示すごとく、転写される一部領域に印刷される。但し、ホログラム箔の転写を安定させるために、加飾フィルム部材20の外周に沿ってロ字状の領域24aも印刷される。なお図18において、黒で塗りつぶされた領域がUV硬化型インク24,24aで印刷された領域を示している。
As shown in FIG. 19 to be described later, the hologram foil is transferred onto a basic symbol (in this embodiment, “butterfly” in FIG. 17 described above) or a part of the periphery thereof. As shown in FIG. 4, the image is printed on a partial area to be transferred. However, in order to stabilize the transfer of the hologram foil, a square-shaped
図13は、シルク印刷された結果、上記UV系特殊インク23の層上の一部にUV硬化型インク24,24aが載った状態の一例を示す断面図である。但し、図13も、加飾フィルム部材20上にシルク印刷された状態を便宜的に表すものであって、図18の印刷結果と正確に対応しているものではない。UV硬化型インク24,24aの厚さは、8(μm)程度である。
FIG. 13 is a cross-sectional view showing an example of a state in which the UV
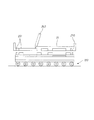
次に工程S3dにおいて、ホログラム箔を転写する。ホログラム箔は、ラミネータ90により、次のようにして、UV硬化型インク24,24aが印刷されている部分に転写される。ここで、ラミネータ90は、図14にて示すごとく、基台91、移動プレート92、支持ローラ93、捲き取りローラ94及び押圧ローラ95を備えている。
Next, in step S3d, the hologram foil is transferred. The hologram foil is transferred by the
移動プレート92は、基台91の上面上に図14にて図示左右方向へ移動可能に載置されている。なお、当該移動プレート92は、図示しない駆動機構により、左方向或いは右方向に移動するように駆動される。
The moving
支持ローラ93は、その軸にて、移動プレート92の直上において、図14にて紙面に直角な方向に沿うように支持されており、当該支持ローラ93は、図14にて図示反時計方向に回転する。
The
巻き取りローラ94は、その軸にて、図14の支持ローラ93の図示左側下方にて、支持ローラ93の軸に平行となるように、移動プレート92の直上にて支持されており、当該巻き取りローラ94は、図14にて図示時計方向に回転するように、回転機構(図示しない)により駆動される。また、押圧ローラ95は、その軸にて、図14の支持ローラ93の図示右側下方にて、巻き取りローラ94よりも下方に位置するように、移動プレート92の直上に支持されており、当該押圧ローラ95は、図14にて図示時計方向に回転するようになっている。
The take-up
このような前提のもと、工程S3cにおいてUV硬化型インク24,24aが印刷された貼着印刷フィルム層70を、図14にて示すごとく、ラミネータ90の移動プレート92上に載置する。この載置は、貼着印刷フィルム層70を移動プレート92と押圧ローラ95との間にて移動プレート92の図14にて図示右側から左側への移動に伴い移動させるように行う。
Under such a premise, the adhesive printed
このようなラミネータ90の構成のもと、ホログラム箔蒸着シートロール25bを図14にて示すごとく支持ローラ93に同軸的に支持する。そして、当該ホログラム箔蒸着シートロール25bの先端部を押圧ローラ95の表面を経由して巻き取りローラ94に巻き付ける。
Under such a configuration of the
しかして、ラミネータ90が作動状態におかれると、移動プレート92が、基台91の上面に沿い図14にて図示左方へ移動する。また、巻き取りローラ94が図14にて図示時計方向に回転すると、ホログラム箔蒸着シートロール25bは、巻き取りローラ94により巻き取られるとともに、移動プレート92の移動に伴い、押圧ローラ95の外表面との摩擦接触のもと当該押圧ローラ95を図14にて図示時計方向に回転させながら、当該押圧ローラ95と貼着印刷フィルム層70との間にて押圧されて貼着印刷フィルム層70と共に左側へ移動していく。
Thus, when the
このとき、このような移動過程において、ホログラム箔蒸着シートロール25bが、押圧ローラ95により、貼着印刷フィルム層70のUV硬化型インク24,24aにその上側から押圧されて、ホログラム箔が転写されていく(図14参照)。これにより、ホログラム箔が、UV硬化型インク24,24aに押圧により転写されつつ、移動プレート92の左方への移動に応じて、貼着印刷フィルム層70と共に移動されていく。
At this time, in such a moving process, the hologram foil vapor-deposited
上述のごとく、ホログラム箔蒸着シートロール25bとして、その表面(転写面)に転写用の糊が付いているものを用いる場合、工程S3bにおいて、加飾フィルム部材20の裏面全体に亘って、ホログラム箔の定着を防止するUV系特殊インク23が印刷されている。従って、加飾フィルム部材20上、UV硬化型インク24,24aが印刷されていない部分は、UV系特殊インク23がホログラム箔蒸着シートロール25bの表面と接触するため、ホログラム箔はこの部分に定着しない。即ち、ホログラム箔は、図19に示すごとく、UV硬化型インク24,24aが印刷されている部分25,25aにのみ定着する。
As described above, when using a hologram foil vapor-deposited
図15は、UV硬化型インク24,24a上にホログラム箔が転写された状態の一例を示す断面図である。但し、図15も、加飾フィルム部材20上にホログラム箔が転写された状態を便宜的に表すものであって、図19の転写結果と正確に対応しているものではない。ホログラム箔25,25aの厚さは、2(μm)程度である。
FIG. 15 is a cross-sectional view showing an example of a state in which the hologram foil is transferred onto the UV
次に工程S3eにおいて、シルク印刷にて、段差を埋める印刷を行う。加飾フィルム部材20上、ホログラム箔が転写された領域とホログラム箔が転写されていない領域の間には、10(μm)程度の段差が生ずる。これは、ホログラム箔が転写された領域25,25aには必ず、UV硬化型インク24,24aが印刷されているため、UV硬化型インクの厚み8(μm)程度とホログラム箔の厚み2(μm)程度を加算した結果が10(μm)程度となるからである。上記工程S3eでは、このような段差を埋めるために、凹んでいる部分に透明なインク、具体的には、UV系特殊インク(樹脂)をシルク印刷にて流し込むようにしている。
Next, in step S3e, printing that fills the step is performed by silk printing. On the
このように段差をなくして加飾フィルム部材20の表面をフラットにするのは、遊技盤の種類によっては、盤面がフラットでなければならないと規定されており、これに対処するためである。しかし、段差といっても、10(μm)程度であるので、規定の範囲内に収まっていれば、この工程S3eを省略してもよい。
The reason why the surface of the
なお、ホログラム箔が転写されたロ字状の領域25a(図19参照)は、前述のごとく、ホログラム箔の転写を安定させるためのものであるので、ホログラム箔が転写された後は必要のないものである。このため、当該領域25aは、後述する切り込み工程S5の処理において切断される。
Note that the square-shaped
以上で、印刷工程S3が終了し、次の粘着層貼着工程S4における処理を行う。この処理にあたり、粘着素材ロール80(図20及び図21参照)を準備する。この粘着素材ロール80は、図20或いは図21にて示すごとく、粘着素材層81、一側分離層82及び他側分離層83を備えている。
Above, printing process S3 is complete | finished and the process in the following adhesion layer sticking process S4 is performed. In this process, an adhesive material roll 80 (see FIGS. 20 and 21) is prepared. As shown in FIG. 20 or FIG. 21, the
当該粘着素材ロール80において、粘着素材層81は、上述した日栄化工株式会社製のWF−D804型アクリル系粘着剤でもって、所定の厚さ50(μm)にて、長手状に形成されている。
In the
一側分離層82は、所定の厚さ25(μm)を有するようにPETでもって形成されており、当該一側分離層82は、その裏面にて、粘着素材層81に沿いその一側面にて貼着されている。他側分離層83は、所定の厚さ75(μm)を有するようにPETでもって形成されており、当該他側分離層83は、その表面にて、粘着素材層81に沿いその他側面にて貼着されている。なお、一側分離層82及び他側分離層83は、PETに限ることなく、ポリエステルであればよく、また、ポリプロピレンを含む熱可塑性樹脂であってもよい。
The one-
しかして、このように準備した粘着素材ロール80を、ラミネータ90aにより、次のようにして、工程S3eにおいて段差の埋められた貼着印刷フィルム層71に貼着する。ここで、ラミネータ90aは、図20にて示すごとく、基台91、移動プレート92、支持ローラ93a、捲き取りローラ94a及び押圧ローラ95aを備えている。なお、ラミネータ90aは、前記図14のラミネータ90に対して、各ローラ93a,94a,95aの配置と機能が若干異なるのみである。基台91と移動プレート92は、両ラミネータ90,90a間で共通する。このため、基台91及び移動プレート92についての説明は省略する。
Thus, the
支持ローラ93aは、その軸にて、移動プレート92の直上において、図20にて紙面に直角な方向に沿うように支持されており、当該支持ローラ93aは、図20にて図示反時計方向に回転する。
The
巻き取りローラ94aは、その軸にて、図20の支持ローラ93aの図示右側下方にて、支持ローラ93aの軸に平行となるように、移動プレート92の直上にて支持されており、当該巻き取りローラ94aは、図20にて図示反時計方向に回転するように、回転機構(図示しない)により駆動される。また、押圧ローラ95aは、その軸にて、支持ローラ93及び巻き取りローラ94aの間において、巻き取りローラ94aよりも下方に位置するように、移動プレート92の直上に支持されており、当該押圧ローラ95aは、図20にて図示時計方向に回転するようになっている。
The take-up roller 94a is supported by the shaft directly above the moving
このような前提のもと、貼着印刷フィルム層71を、図20にて示すごとく、ラミネータ90aの移動プレート92上に載置する。この載置は、貼着印刷フィルム層71を移動プレート92と押圧ローラ95aとの間にて移動プレート92の図20にて図示右側から左側への移動に伴い移動させるように行う。
Under such a premise, the adhesive printed
このようなラミネータ90aの構成のもと、粘着素材ロール80を図20にて示すごとく支持ローラ93aに同軸的に支持する。そして、当該粘着素材ロール80の一側分離層82の先端部を粘着素材層81の先端部から分離した後、当該一側分離層82をその先端部から捲き取りローラ94aに図20にて反時計方向巻きに捲き付ける。一方、粘着素材ロール80の粘着素材層81及び他側分離層83をその各先端部から押圧ローラ95と貼着印刷フィルム層71との間に押し込む。このとき、他側分離層83は、その先端部にて、粘着素材層81の先端部の上側に位置し、粘着素材層81は、その先端部にて、貼着印刷フィルム層71の加飾フィルム部材20上に位置する。従って、貼着印刷フィルム層71は、その保護フィルム21にて、移動プレート92上に載置されている。
Under such a configuration of the
しかして、ラミネータ90aが作動状態におかれると、移動プレート92が、基台91の上面に沿い図20にて図示左方へ移動する。また、巻き取りローラ94aが図20にて図示反時計方向に回転すると、粘着素材ロール80においては、一側分離層82が、粘着素材層81から順次分離されつつ巻き取りローラ94aにより巻き取られるとともに、粘着素材層81が、一側分離層82から分離されつつ、他側分離層83と共に、移動プレート92の移動に伴い、押圧ローラ95aの外表面との摩擦接触のもと当該押圧ローラ95aを図20にて図示時計方向に回転させながら、当該押圧ローラ95aと貼着印刷フィルム層71との間にて押圧されて貼着印刷フィルム層71と共に左側へ移動していく。
Thus, when the
このとき、このような移動過程において、粘着素材層81が、押圧ローラ95aにより、貼着印刷フィルム層71の加飾フィルム部材20にその上側から押圧されて貼着されていく(図20参照)。これにより、粘着素材層81が、加飾フィルム部材20に押圧により貼着されつつ、加飾フィルム部材20と一体となって、移動プレート92の左方への移動に応じて、貼着印刷フィルム層71と共に移動されていく。
At this time, in such a moving process, the
このような過程において、粘着素材層81が、その加飾フィルム部材20の右端部に対する対応部位にて、当該加飾フィルム部材20の右端部に押圧により貼着されると、粘着素材ロール80が、他側分離層83及び粘着素材層81の加飾フィルム部材20の右端部に対する対応部位にて、ラミネータ90aによりそのカッター(図示しない)でもって切断される。
In such a process, when the
このとき、粘着素材層81が粘着層30として切断され、他側分離層83が、粘着層用他側分離層83aとして切断される。しかして、上述のような粘着素材ロール80の切断でもって、粘着層用他側分離層83a、粘着層30並びに貼着印刷フィルム層71の加飾フィルム部材20及び保護フィルム21からなる4層貼着体100(図22参照)が形成される。なお、4層貼着体100を構成する加飾フィルム部材20には、上記印刷工程S3において、各種インク及びホログラム箔からなる層が形成されているが、図22等では、当該層は図示していない。
At this time, the
上述のような切断は、新たな貼着印刷フィルム層71毎になされて、対応の貼着印刷フィルム層71と共に、4層貼着体100(図22参照)として形成される。
The cutting as described above is performed for each new adhesive
然る後、次の切り込み工程S5の処理がなされる。この処理では、4層貼着体100が、保護フィルム21以外の構成部位(粘着層用他側分離層83a、粘着層30及び加飾フィルム部材20)にて、次のようにして、トムソン抜き型110でもって、切り込まれる。
Thereafter, the next cutting step S5 is performed. In this treatment, the four-
トムソン抜き型110は、図23にて示すごとく、板状型本体111、環状切りこみ刃112及び環状切断刃113を備えている。環状切りこみ刃112は、所定の環形状、即ち、遊技基板10の中央開口部11の内周面に沿う環形状でもって、板状型本体111の下面から下方へ突出するように形成されている。
As shown in FIG. 23, the Thomson punching die 110 includes a plate-
ここで、当該環状切りこみ刃112の縦断面形状は、図23にて示すごとく、板状型本体111の下面からくさび状にて鋭く末すぼまり状に立ち下がる形状となっている。なお、当該切りこみ刃112は、その外周面にて板状型本体111の下面から下方へ垂直状に立ち下がっており、当該切り込み刃112の内周面は、板状型本体111の下面から下方へかつ切りこみ刃112の外周面に達するように傾斜状に立ち下がることで、上記末すぼまり状の立ち下がり形状となっている。
Here, as shown in FIG. 23, the longitudinal sectional shape of the
また、環状切断刃113は、所定の環形状、即ち、化粧シートSの外周面形状に対応する環形状でもって、環状切りこみ刃112の外周側にて、板状型本体111の下面から下方へ突出するように形成されている。
Further, the
ここで、当該環状切断刃113の縦断面形状は、図23にて示すごとく、板状型本体111の下面からくさび状にて鋭く末すぼまり状に立ち下がる形状となっている。但し、環状切断刃113の板状型本体111の下面からの突出長さは、環状切りこみ刃112の板状型本体111の下面からの突出長さに比べて、保護フィルム21の厚さ分だけ長くなっている。
Here, as shown in FIG. 23, the longitudinal cross-sectional shape of the
なお、当該環状切断刃113は、その内周面にて板状型本体111の下面から下方へ垂直状に立ち下がっており、当該切り込み刃112の外周面は、板状型本体111の下面から下方へかつ環状切断刃113の内周面に達するように傾斜状に立ち下がることで、上記末すぼまり状の立ち下がり形状となっている。
Note that the
しかして、このようなトムソン抜き型110の構成のもと、4層貼着体100が、その保護フィルム21から、作業台Mの上面上に載置される。ついで、トムソン抜き型110が、その切りこみ刃112の先端部にて、4層貼着体100を介し、遊技基板10の中央開口部11に同心的に対応して位置するように、4層貼着体100の粘着層用他側分離層83a上に載置される。
Under the configuration of the Thomson punching die 110, the four-
然る後、トムソン抜き型110が、その板状型本体111にて、プレス機(図示しない)により、下方(図23の図示矢印方向)に沿い作業台Mの上面に向けて押圧される。これに伴い、トムソン抜き型110が、その環状切断刃113にて、4層貼着体100を、化粧シートSの外周面形状に対応するように粘着層用他側分離層83aから保護フィルム21にかけて切断するとともに、環状切りこみ刃112にて、4層貼着体100を、遊技基板10の中央開口部11の内周面形状に対応するように粘着層用他側分離層83aから加飾フィルム部材20にかけて、順次、切り込む。
Thereafter, the Thomson punching die 110 is pressed toward the upper surface of the work table M along the lower side (in the direction of the arrow in FIG. 23) by the press machine (not shown) in the plate-
これにより、4層貼着体100は、化粧シートSの外周面形状に切断されるとともに、保護フィルム21を除き、加飾フィルム部材20、粘着層30、粘着層用他側分離層83aのうち遊技基板10の中央開口部11に対する各対応部位にて、切り込まれる(図23参照)。このとき、切りこみ刃112による切り込み形状は、遊技基板10の中央開口部11の内周面に対応する環状形状となっており、また、環状切断刃113による切断形状は、化粧シートSの外周面形状となっている。
Thereby, while the 4
4層貼着体100のうち、化粧シートSを切断した後の残りの部分に、上述のロ字状の領域24aが含まれる。換言すると、化粧シートSの外周面形状の外側に、上記工程S3cにおいて、ロ字状の領域24aをシルク印刷しておく必要がある。こうすることで、不要となったロ字状の領域24a、即ち、転写を安定させる目的のためだけに印刷され、ホログラム箔が転写された後に不要となったロ字状の領域24aを化粧シートSから自動的に削除することができる。なお、ホログラム箔の転写を安定させるために印刷する領域の形状は、上記ロ字状に限らず、コ字状やL字状等の他の形状であってもよい。但し、帯状の領域が、少なくとも2領域(平行または直角に配置)あった方が、転写の安定のためには好ましい。
Of the four-
次の遊技基板への貼着工程S6においては、上述のように切断加工及び切り込み加工がなされた4層貼着体100(以下、切断切り込み加工済み4層貼着体100aともいう)が、次のようにして、ビックラダー株式会社製専用貼り機120でもって、遊技基板10に貼り合わされる。
In the next game board sticking step S6, the four-
ここで、専用貼り機120は、図24にて示すごとく、基台121と、L字板状移動部材122と、ベルト駆動機構123と、押圧ローラ124とを備えている。L字板状移動部材122は、その板状脚部122aにて、基台121にその上面から下方に向け凹状に形成された凹所(図示しない)に沿い、ベルト駆動機構123による駆動に応じて、図24にて図示左右方向に移動可能に支持されて上方へ延出している。
Here, as shown in FIG. 24, the
また、L字板状移動部材122の板状腕部122bは、板状脚部122aの延出端部から図24にて図示左方へL字状に折れ曲がって延出しており、当該板状腕部122bの延出端部には、押圧ローラ124が、その軸にて、図24にて紙面の手前から奥に向くように支持されている。ここで、当該押圧ローラ124が、その外周面にて、後述のように基台121上に載置される遊技基板10の表面に沿い当接して回転するように、板状腕部122bの基台121の上面からの延出高さが設定されている。
Further, the plate-
このような専用貼り機120の構成のもと、遊技基板10を、図24にて示すごとく、L字板状移動部材122の左側に位置するように、基台10の上面上に載置する。このとき、遊技基板10が、その図24にて図示右端部にて、押圧ローラ124の下端部直下近傍に位置するように、載置される。
Under the configuration of the
然る後、切断切り込み加工済み4層貼着体100aにおいて、粘着層用他側分離層83aを、把持して、図24にて示すごとく、剥がしながら、残りの保護フィルム21、加飾フィルム部材20及び粘着層30を、その各右端部にて、遊技基板10の表面の右端部と押圧ローラ124の下端部との間に押し付ける。
Thereafter, in the four-layer stuck
ついで、L字板状移動部材122が基台121に沿い左方へ移動するようにベルト駆動機構123でもって駆動される。すると、L字板状移動部材122の左方への移動に伴い、保護フィルム21、加飾フィルム部材20及び粘着層30が、共に、遊技基板10の表面に、押圧ローラ124により所定の圧力範囲内の圧力でもって押圧される。
Next, the L-shaped plate-shaped moving
本実施形態において、上記所定の圧力範囲は、粘着層30の遊技基板10に対する粘着力を良好に確保し得る範囲以内の圧力であればよく、本実施形態では、例えば、3(kg/cm2)〜4.7(kg/cm2)をいう。なお、当該圧力の上限は、4.7(kg/cm2)に限ることなく、高い程好ましいが、粘着層30の遊技基板10に対する押圧後その開放の際に粘着層30の外形形状を原形状に復帰させ得る程度に設定するとよい。また、当該圧力の下限は、3(kg/cm2)に限らないが、粘着層30の遊技基板10に対する粘着力を良好に確保し得るように設定するとよい。
In the present embodiment, the predetermined pressure range may be a pressure within a range in which the adhesive force of the
これにより、粘着層30が、その粘着作用により、図25にて示すごとく、遊技基板10の表面に粘着される。このことは、保護フィルム21及び加飾フィルム部材20が、粘着層30でもって、遊技基板10の表面に貼着されることを意味する。
Thereby, the
ここで、上述のごとく切断切り込み加工済み4層貼着体100aのうち切り込み刃112の中空部に対する対応部位(以下、切り込み対応部位101という)が、遊技基板10の中央開口部11の中空部に対応するように、加飾フィルム部材20が、粘着層30でもって、遊技基板10の表面に貼着される。
Here, in the four-
このような貼着がなされた後、次の保護フィルム剥がし工程S7の処理がなされる。この処理では、保護フィルム21が、手作業により、図26にて図示矢印にて示すごとく、加飾フィルム部材20から剥がされると、切り込み対応部位101が、図26にて示すごとく、保護フィルム21と一緒に切断切り込み加工済み4層貼着体100aのうち切り込み対応部位101以外の部位から除去される。これにより、化粧シートSが、図1にて示すごとく遊技基板10に貼着されて、当該遊技基板10と共に、遊技盤Bとして製造される。
After such sticking, the next protective film peeling step S7 is performed. In this process, when the
ところで、上述のような遊技盤Bの製造直後は、化粧シートSの遊技基板10に対する貼着の直後に対応する。このような段階にて、検査によって、例えば、皺が化粧シートSに形成されていることが発見されたり、或いは、ゴミが化粧シートSと遊技基板10との間に混入していることが発見されたりすると、製造された遊技盤は、従来は、品質不良であるとして廃棄処分の対象となるのが原則である。
By the way, immediately after the manufacture of the game board B as described above corresponds to immediately after the decorative sheet S is attached to the
しかしながら、上述のように製造された遊技盤において用いられている遊技基板10は、従来の廉価なベニヤからなるものではなく、PC樹脂からなる高価な遊技基板である。従って、このような高価な遊技基板が、製造された遊技盤が上述のような理由のために、品質不良として廃棄されてしまうのは、経済性に欠けるのは勿論のこと、省資源の観点からも好ましくない。このため、当該遊技基板の再利用を可能にすることが要請される。
However, the
然るに、上述したごとく、遊技基板10と化粧シートSとの貼り合わせ直後の粘着力は、化粧シートSを遊技基板10から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低い粘着力であることから、上記貼り合わせ直後において、化粧シートSを遊技基板10から剥がすことで、当該遊技基板10が再利用可能となる。
However, as described above, the adhesive force immediately after bonding of the
ここで、上述した遊技基板10と化粧シートSとの貼り合わせ直後とは、当該遊技基板10と化粧シートSとの貼り合わせの後の所定の短時間(例えば、20(分))以内をいう。これは、表1にて示すごとく、雰囲気温度10(℃)では、粘着力が、20(分)以内においては、化粧シートSを遊技基板10から痕跡を残すことなくきれいにかつ容易に剥がし得る程度に低いことに基づく。
Here, “immediately after the
そこで、このように再利用可能となった遊技基板10を再び用いて、上述のような製造工程を経て、新たな化粧シートSを遊技基板10に適正に貼り直すことで、遊技基板10の中央開口部11の開口面積が広くても、新たな化粧シートSを遊技基板10に良好に貼り直すことができ、その結果、良好な遊技盤を新たに製造し得る。このように、遊技基板の再利用でもって無駄を無くすることで、省資源に貢献するとともに、遊技盤としての製造コストの不必要な増大をも防止し得る。
Therefore, the
また、上述のように新たに製造した遊技盤は、上記常温の雰囲気温度環境の中で、そのまま、24(時間)放置しておけば、粘着層30の粘着力が上述の通り強くなり、新たな化粧シートSを遊技基板10に対し硬く貼着することができる。
In addition, if the game board newly manufactured as described above is left as it is for 24 (hours) in the ambient temperature environment described above, the adhesive strength of the
なお、上述したごとく、遊技基板10、加飾フィルム部材20及び粘着層30の各形成材料は、透明であることから、遊技盤の前側から遊技盤の裏面側を当該遊技盤を通して視認可能であることはいうまでもない。
As described above, since the formation materials of the
さらに、加飾フィルム部材20には、従来の加飾である基本図柄の印刷(図17参照)に加え、新しい加飾であるホログラム箔の転写もなされているので、新しい加飾、具体的には、レーザー光線がホログラム箔に照射され、ホログラム箔の柄が浮き出るといった新しい加飾による見映えのさらなる向上を図ることができる。
Furthermore, since the
なお、本発明の実施にあたり、上記実施形態に限ることなく、次のような種々の変形例が挙げられる。
(1)本発明の実施にあたり、上記実施形態にて述べた製造工程の処理は、常温の10(℃)の環境で行うことに代えて、10(℃)以外の温度、例えば、0(℃)以上20(℃)未満の環境で行なうようにしてもよい。
(2)本発明の実施にあたり、上記実施形態のように複数の遊技盤を製造するのではなく、単一の遊技盤を製造するにあたり本発明を適用してもよい。
(3)本発明の実施にあたり、上記実施形態において、加飾フィルム部材の裏面に直接、基本図柄及びホログラム箔を印刷及び転写するのに代えて、加飾フィルム部材をベースフィルム層と印刷フィルム層とから構成し、基本図柄及びホログラム箔を印刷及び転写した印刷フィルム層をベースフィルム層に貼着するようにしてもよい。
(4)本発明の実施にあたり、上記実施形態にて述べた粘着層30の形成材料は、日栄化工株式会社製のWF−D804型アクリル系粘着剤に限ることなく、当該日栄化工株式会社製のD−8048048型アクリル系粘着剤、或いは上記WF−D804型アクリル系粘着剤と類似する粘着力特性を有する粘着剤であってもよい。
(5)本発明の実施にあたり、上記実施形態にて述べた化粧シートは、対応の各遊技基板にその裏面側から貼着するようにしてもよい。
(6)本発明の実施にあたり、上記実施形態にて述べた加飾フィルム部材20は、PETに限ることなく、ポリカーボネート、アクリル系樹脂、キャブロイド(登録商標)や塩化ビニル樹脂で形成してもよく、また、上記第2実施形態にて述べた保護フィルムは、PETに限ることなく、例えば、ポリプロピレン(PP)、ポリカーボネート(PC)、アクリル系樹脂、ポリ塩化ビニルでもって形成するようにしてもよい。
In carrying out the present invention, the following various modifications are possible without being limited to the above embodiment.
(1) In carrying out the present invention, the process of the manufacturing process described in the above embodiment is performed in an environment of 10 (° C.) at room temperature, and a temperature other than 10 (° C.), for example, 0 (° C. ) You may make it carry out in the environment below 20 (degreeC).
(2) In practicing the present invention, the present invention may be applied to the production of a single game board instead of producing a plurality of game boards as in the above embodiment.
(3) In carrying out the present invention, in the above embodiment, instead of printing and transferring the basic design and the hologram foil directly on the back surface of the decorative film member, the decorative film member is replaced with a base film layer and a printed film layer. The printed film layer on which the basic design and the hologram foil are printed and transferred may be attached to the base film layer.
(4) In carrying out the present invention, the material for forming the pressure-
(5) In carrying out the present invention, the decorative sheet described in the above embodiment may be attached to each corresponding game board from the back side.
(6) In carrying out the present invention, the
また、上記実施形態にて述べた加飾フィルムロール40は、PETに限らず、一般的には、ポリエステル系樹脂或いは当該ポリエステル系樹脂でもって形成するようにしてもよく、また、上記各実施形態にて述べた保護フィルムロール50は、PETに限らず、一般的にはポリエステル系樹脂でもって形成するようにしてもよい。また、加飾フィルムロール40や保護フィルムロール50は、ポリエステル系樹脂に限ることなく、例えば、ポリプロピレン(PP)、ポリカーボネート(PC)、アクリル系樹脂、塩化ビニル樹脂或いはキャブロイド(登録商標)等のセルロース系樹脂その他の熱可塑性樹脂でもって形成するようにしてもよい。
(7)本発明の実施にあたり、上記各実施形態にて述べた遊技盤の製造にあたり、図3及び図26の製造工程において、単一の遊技盤を製造するようにしてもよい。
In addition, the
(7) In practicing the present invention, a single game board may be manufactured in the manufacturing process of FIGS. 3 and 26 in manufacturing the game board described in the above embodiments.
この場合、上記実施形態において、遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する中央開口部11を有するように形成してなる透明性ポリカーボネート樹脂製遊技基板10を予め準備し、
かつ、ポリカーボネート樹脂製遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層30を予め準備して、
ポリエステル系樹脂製保護フィルム21を、その裏面にて、粘着層30と共に化粧シートを構成する透明性ポリエステル系樹脂製加飾フィルム部材20にその表面にて貼着する第1工程と、
当該第1工程における上記貼着後、加飾フィルム部材20の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な特殊インクを印刷し、当該特殊インクの印刷された部分にホログラム箔を転写させる第2工程と、
粘着層30を加飾フィルム部材20にその裏面側から貼着する第3工程と、
粘着層30、加飾フィルム部材20及び保護フィルム21からなる貼着体のうち遊技基板10の中央開口部11の内周面に対する対応部位を、保護フィルム21を除き粘着層30から加飾フィルム部材20にかけて切り込み、切り込み済み対応部位として形成する第4工程と、
上記切り込み済みの保護フィルム21、加飾フィルム部材20及び粘着層30からなる切り込み済み貼着体を、その粘着層30にて、遊技基板10の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
保護フィルム21を加飾フィルム部材20から剥がしながら、切り込み済み貼着体の加飾フィルム部材20及び粘着層30のうち上記切り込み済み対応部位の内側部位を保護フィルム21と共に一体的に除去する第6工程とを備えて、
上記第1〜第6の工程を上記所定の雰囲気温度の環境内で行い、第6工程後所定の短時間内に化粧シートSの異常或いは粘着層30と遊技基板10との間に異物の混入が発見されたとき、化粧シートSを遊技基板10から剥がして新たな化粧シートを遊技基板10に上記第1〜第6の工程を経て貼着し直すことで遊技盤を新たに製造するようにしてもよい。
In this case, in the above embodiment, as a gaming board, a transparent polycarbonate
In addition, it is a transparent pressure-sensitive adhesive that exhibits an adhesive property that is low immediately after the sticking when it is stuck on the surface of a polycarbonate resin game board and increases with the passage of time in an environment of a predetermined atmospheric temperature. An
A first step of sticking the polyester resin
After the sticking in the first step, a predetermined pattern is formed on the back surface of the
A third step of adhering the
A part corresponding to the inner peripheral surface of the
The above-mentioned cut-in stuck body composed of the cut-in
The 6th which removes the inner side part of the above-mentioned cut corresponding part together with
The first to sixth steps are performed in the environment of the predetermined ambient temperature, and after the sixth step, an abnormality of the decorative sheet S or a foreign matter mixed between the
また、上記実施形態において、遊技基板として、各種遊技部品のうちの演出表示装置を組み付けるに要する中央開口部11を有するように形成してなる透明性ポリカーボネート樹脂製遊技基板10を予め準備し、
かつ、ポリカーボネート樹脂製遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層30を予め準備して、
ポリエステル系樹脂製保護フィルム21を、その裏面にて、粘着層30と共に化粧シートを構成する透明性ポリエステル系樹脂製加飾フィルム部材20にその表面にて貼着する第1工程と、
当該第1工程における上記貼着後、加飾フィルム部材20の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な第1特殊インクを印刷し、当該第1特殊インクの印刷された部分にホログラム箔を転写させ、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インクを印刷にて流し込む第2工程と、
粘着層30を加飾フィルム部材20にその裏面側から貼着する第3工程と、
粘着層30、加飾フィルム部材20及び保護フィルム21からなる貼着体のうち遊技基板10の中央開口部11の内周面に対する対応部位を、保護フィルム21を除き粘着層30から加飾フィルム部材20にかけて切り込み、切り込み済み対応部位として形成する第4工程と、
上記切り込み済みの保護フィルム21、加飾フィルム部材20及び粘着層30からなる切り込み済み貼着体を、その粘着層30にて、遊技基板10の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
保護フィルム21を加飾フィルム部材20から剥がしながら、切り込み済み貼着体の加飾フィルム部材20及び粘着層30のうち上記切り込み済み対応部位の内側部位を保護フィルム21と共に一体的に除去する第6工程とを備えて、
上記第1〜第6の工程を上記所定の雰囲気温度の環境内で行い、第6工程後所定の短時間内に化粧シートSの異常或いは粘着層30と遊技基板10との間に異物の混入が発見されたとき、化粧シートSを遊技基板10から剥がして新たな化粧シートを遊技基板10に上記第1〜第6の工程を経て貼着し直すことで遊技盤を新たに製造するようにしてもよい。
(8)本発明の実施にあたり、遊技基板、粘着層及び加飾フィルム部材の各形成材料は、無色透明に限らず、有色透明であってもよく、要するに透光性を有すればよい。
(9)本発明の実施にあたり、化粧シートは、上記実施形態とは異なり、遊技基板の裏面に貼着するようにしてもよい。
(10)本発明の実施にあたり、上記実施形態にて述べたラミネータ90aにおいて、上記実施形態とは異なり、支持ローラ93aを押圧ローラ95aを基準に図20にて図示右側に配設するとともに、巻き取りローラ94aを、押圧ローラ95aを基準に図20にて図示左側に配設するようにして、支持ローラ93aの図20にて図示時計方向への回転のもとに、粘着素材ローラ80の一側分離層82を、巻き取りローラ94aによりその時計方向への回転のもとに巻き取り、粘着素材層81及び他側分離層83を、押圧ローラ95aによりその図20にて図示反時計方向への回転のもとに押圧するようにしてもよい。このとき、移動プレート92は、上記実施形態とは異なり、図20にて図示右方へ移動する。
(11)本発明の実施にあたり、上記実施形態にて述べた専用貼り機120は、ビックラダー株式会社製に限ることなく、例えば、クライムプロダクツ株式会社製シール方式精密枚葉貼り合わせ機であってもよい。
(12)本発明の実施にあたり、上記実施形態にて述べた遊技基板の形成材料は、透明のポリカーボネート樹脂に限ることなく、例えば、透明のアクリル樹脂であってもよい。
In the above embodiment, as a gaming board, a
In addition, it is a transparent pressure-sensitive adhesive that exhibits an adhesive property that is low immediately after the sticking when it is stuck on the surface of a polycarbonate resin game board and increases with the passage of time in an environment of a predetermined atmospheric temperature. An
A first step of sticking the polyester resin
After the pasting in the first step, a predetermined pattern is formed on the back surface of the
A third step of adhering the
A part corresponding to the inner peripheral surface of the
The above-mentioned cut-in stuck body composed of the cut-in
The 6th which removes the inner side part of the above-mentioned cut corresponding part together with
The first to sixth steps are performed in the environment of the predetermined ambient temperature, and after the sixth step, an abnormality of the decorative sheet S or a foreign matter mixed between the
(8) In carrying out the present invention, each forming material of the game board, the adhesive layer, and the decorative film member is not limited to being colorless and transparent, and may be colored and transparent, in other words, only has translucency.
(9) In carrying out the present invention, the decorative sheet may be adhered to the back surface of the game board, unlike the above embodiment.
(10) In carrying out the present invention, in the
(11) In carrying out the present invention, the
(12) In implementing the present invention, the game board forming material described in the above embodiment is not limited to a transparent polycarbonate resin, and may be a transparent acrylic resin, for example.
10…遊技基板、11…中央開口部、20…加飾フィルム部材、
21…保護フィルム、30…粘着層、40…加飾フィルム部材ロール、
50…保護フィルムロール、60…フィルム貼着ロール体、
60a…貼着フィルム層、80…粘着素材ロール、81…粘着素材層、
82…一側分離層、83…他側分離層、100…4層貼着体、
100a…切り込み済み4層貼着体、S1…保護フィルムロール貼着工程、
S2…切断工程、S4…粘着層貼着工程、S5…切り込み工程、
S6…遊技基板への貼着工程、S7…保護フィルム剥がし工程。
10 ... gaming board, 11 ... central opening, 20 ... decorative film member,
21 ... Protective film, 30 ... Adhesive layer, 40 ... Decorated film member roll,
50 ... Protective film roll, 60 ... Film sticking roll body,
60a ... Adhesive film layer, 80 ... Adhesive material roll, 81 ... Adhesive material layer,
82 ... one side separation layer, 83 ... other side separation layer, 100 ... four-layer sticking body,
100a ... Cut four-layer sticker, S1 ... Protective film roll sticking step,
S2 ... Cutting step, S4 ... Adhesive layer attaching step, S5 ... Cutting step,
S6 ... Sticking process to game board, S7 ... Protective film peeling process.
Claims (16)
前記遊技基板は、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板であり、
前記化粧シートは、その裏面に所定の図柄が形成された後、当該裏面の一部に印刷された、ホログラム箔を付着させるための透明な特殊インクを介してホログラム箔が転写されたものであり、
前記粘着層は、前記遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなることを特徴とする遊技盤。 A game board in which a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine are attached via an adhesive layer,
The game board is a game board made of a transparent polycarbonate resin or a transparent acrylic resin formed to have an opening necessary for assembling the effect display device among the various game parts,
The decorative sheet is formed by transferring a hologram foil via a transparent special ink printed on a part of the back surface, after a predetermined pattern is formed on the back surface, for attaching the hologram foil. ,
The pressure-sensitive adhesive layer is a transparent pressure-sensitive adhesive that exhibits an adhesive property that is low immediately after the bonding and increases with the passage of time when it is attached to the surface of the game board in an environment of a predetermined atmospheric temperature. A game board characterized by being formed.
前記遊技基板は、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板であり、
前記化粧シートは、その裏面に所定の図柄が形成された後、当該裏面の一部に印刷された、ホログラム箔を付着させるための透明な第1特殊インクを介してホログラム箔が転写され、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インクが印刷にて流し込まれたものであり、
前記粘着層は、前記遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなることを特徴とする遊技盤。 A game board in which a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine are attached via an adhesive layer,
The game board is a game board made of a transparent polycarbonate resin or a transparent acrylic resin formed to have an opening necessary for assembling the effect display device among the various game parts,
After the predetermined pattern is formed on the back surface of the decorative sheet, the hologram foil is transferred via a transparent first special ink printed on a part of the back surface for attaching the hologram foil, The second special ink transparent to the portion where the hologram foil is not transferred in order to fill the level difference between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred to flatten the surface. Was poured in by printing,
The pressure-sensitive adhesive layer is a transparent pressure-sensitive adhesive that exhibits an adhesive property that is low immediately after the bonding and increases with the passage of time when it is attached to the surface of the game board in an environment of a predetermined atmospheric temperature. A game board characterized by being formed.
前記遊技基板として、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板を予め準備し、
かつ、当該遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層を予め準備して、
第1熱可塑性樹脂製の保護フィルムを、その裏面にて、前記粘着層と共に前記化粧シートを構成する透明の第2熱可塑性樹脂製の加飾フィルム部材にその表面にて貼着する第1工程と、
当該第1工程における前記貼着後、前記加飾フィルム部材の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な特殊インクを印刷し、当該特殊インクの印刷された部分にホログラム箔を転写させる第2工程と、
前記粘着層を前記加飾フィルム部材にその裏面側から貼着する第3工程と、
前記粘着層、前記加飾フィルム部材及び前記保護フィルムからなる貼着体を、その前記遊技基板の前記開口部の内周面に対応する切り込み位置にて、前記保護フィルムを除き前記粘着層から前記加飾フィルム部材にかけて切り込み、切り込み貼着体として形成する第4工程と、
前記切り込み貼着体を、その粘着層にて、前記遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
前記保護フィルムを前記加飾フィルム部材から剥がしながら、前記切り込み貼着体のうち前記切り込み位置の内側部位を前記保護フィルムと共に一体的に除去する第6工程とを備えて、
前記第1〜第6の工程を前記所定の雰囲気温度の環境内で行い、前記第6工程後所定の短時間内に前記化粧シートの異常或いは前記粘着層と前記遊技基板との間に異物の混入が発見されたとき、前記化粧シートを前記遊技基板から剥がして新たな化粧シートを前記遊技基板に前記第1〜第6の工程を経て貼着し直すことで製造するようにしたことを特徴とする遊技盤の製造方法。 In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As the gaming board, a gaming board made of transparent polycarbonate resin or transparent acrylic resin formed to have an opening necessary for assembling the effect display device of the various gaming parts is prepared in advance.
And when it is attached to the surface of the game board, it is formed with a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. Prepared in advance,
The 1st process of sticking the protective film made from the 1st thermoplastic resin on the surface to the decoration film member made from the transparent 2nd thermoplastic resin which constitutes the above-mentioned decorative sheet with the above-mentioned adhesion layer on the back side When,
After the sticking in the first step, a predetermined pattern is formed on the back surface of the decorative film member, and a transparent special ink for adhering the hologram foil is printed on a part of the back surface. A second step of transferring the hologram foil to the printed part of
A third step of adhering the adhesive layer to the decorative film member from the back side;
The adhesive body comprising the adhesive layer, the decorative film member, and the protective film is removed from the adhesive layer except for the protective film at a cutting position corresponding to the inner peripheral surface of the opening of the game board. Cutting over the decorative film member, the fourth step to form as a cut sticking body,
A fifth step in which the cut and stuck body is adhered to the surface of the game board by pressing with a pressure within a predetermined pressure range in the adhesive layer;
A sixth step of integrally removing the inner portion of the cut position together with the protective film while peeling off the protective film from the decorative film member,
The first to sixth steps are performed in the environment of the predetermined ambient temperature, and after the sixth step, there is an abnormality of the decorative sheet or a foreign matter between the adhesive layer and the game board within a predetermined short time. When mixing is found, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to sixth steps and manufactured. A game board manufacturing method.
前記第4工程において、当該切り込みと併せて、ホログラム箔が転写された前記帯状の領域を含む領域を当該加飾フィルム部材から切断して、前記切り込み貼着体の外周面形状を前記遊技基板の外周面形状に合わせることを特徴とする請求項4または5に記載の遊技盤の製造方法。 In the second step, when printing a transparent special ink for adhering the hologram foil, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fourth step, an area including the band-shaped area to which the hologram foil has been transferred is cut from the decorative film member together with the notch, and the outer peripheral surface shape of the notch sticking body is changed to that of the game board. The game board manufacturing method according to claim 4, wherein the game board is matched to an outer peripheral surface shape.
前記遊技基板として、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板を予め準備し、
かつ、当該遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤でもって形成してなる粘着層を予め準備して、
第1熱可塑性樹脂製の保護フィルムを、その裏面にて、前記粘着層と共に前記化粧シートを構成する透明の第2熱可塑性樹脂製の加飾フィルム部材にその表面にて貼着する第1工程と、
当該第1工程における前記貼着後、前記加飾フィルム部材の裏面に所定の図柄を形成し、当該裏面の一部に、ホログラム箔を付着させるための透明な第1特殊インクを印刷し、当該第1特殊インクの印刷された部分にホログラム箔を転写させ、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インクを印刷にて流し込む第2工程と、
前記粘着層を前記加飾フィルム部材にその裏面側から貼着する第3工程と、
前記粘着層、前記加飾フィルム部材及び前記保護フィルムからなる貼着体を、その前記遊技基板の前記開口部の内周面に対応する切り込み位置にて、前記保護フィルムを除き前記粘着層から前記加飾フィルム部材にかけて切り込み、切り込み貼着体として形成する第4工程と、
前記切り込み貼着体を、その粘着層にて、前記遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第5工程と、
前記保護フィルムを前記加飾フィルム部材から剥がしながら、前記切り込み貼着体のうち前記切り込み位置の内側部位を前記保護フィルムと共に一体的に除去する第6工程とを備えて、
前記第1〜第6の工程を前記所定の雰囲気温度の環境内で行い、前記第6工程後所定の短時間内に前記化粧シートの異常或いは前記粘着層と前記遊技基板との間に異物の混入が発見されたとき、前記化粧シートを前記遊技基板から剥がして新たな化粧シートを前記遊技基板に前記第1〜第6の工程を経て貼着し直すことで製造するようにしたことを特徴とする遊技盤の製造方法。 In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As the gaming board, a gaming board made of transparent polycarbonate resin or transparent acrylic resin formed to have an opening necessary for assembling the effect display device of the various gaming parts is prepared in advance.
And when it is attached to the surface of the game board, it is formed with a transparent adhesive that exhibits an adhesive strength characteristic that is low immediately after the attachment and increases with the passage of time in a predetermined ambient temperature environment. Prepared in advance,
The 1st process of sticking the protective film made from the 1st thermoplastic resin on the surface to the decoration film member made from the transparent 2nd thermoplastic resin which constitutes the above-mentioned decorative sheet with the above-mentioned adhesion layer on the back side When,
After the sticking in the first step, a predetermined pattern is formed on the back surface of the decorative film member, and a transparent first special ink for attaching a hologram foil is printed on a part of the back surface, To transfer the hologram foil to the printed portion of the first special ink, and to fill the level difference between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred to flatten the surface A second step of pouring a transparent second special ink into a portion where the hologram foil is not transferred to
A third step of adhering the adhesive layer to the decorative film member from the back side;
The adhesive body comprising the adhesive layer, the decorative film member, and the protective film is removed from the adhesive layer except for the protective film at a cutting position corresponding to the inner peripheral surface of the opening of the game board. Cutting over the decorative film member, the fourth step to form as a cut sticking body,
A fifth step in which the cut and stuck body is adhered to the surface of the game board by pressing with a pressure within a predetermined pressure range in the adhesive layer;
A sixth step of integrally removing the inner portion of the cut position together with the protective film while peeling off the protective film from the decorative film member,
The first to sixth steps are performed in the environment of the predetermined ambient temperature, and after the sixth step, there is an abnormality of the decorative sheet or a foreign matter between the adhesive layer and the game board within a predetermined short time. When mixing is found, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to sixth steps and manufactured. A game board manufacturing method.
前記第4工程において、当該切り込みと併せて、ホログラム箔が転写された前記帯状の領域を含む領域を当該加飾フィルム部材から切断して、前記切り込み貼着体の外周面形状を前記遊技基板の外周面形状に合わせることを特徴とする請求項7または8に記載の遊技盤の製造方法。 In the second step, when printing the first special ink, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fourth step, an area including the band-shaped area to which the hologram foil has been transferred is cut from the decorative film member together with the notch, and the outer peripheral surface shape of the notch sticking body is changed to that of the game board. The game board manufacturing method according to claim 7, wherein the game board is matched to the outer peripheral surface shape.
前記遊技基板として、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板を予め準備し、
第1熱可塑性樹脂製の長手状フィルム体からなる保護フィルムロール及び透明の第2熱可塑性樹脂製の長手状フィルム体からなる加飾フィルム部材ロールを予め準備し、
かつ、前記遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤を粘着素材とする粘着素材層と、当該粘着素材層の一側面に沿い貼着してなるポリエステル系樹脂製の長手状一側分離層と、前記粘着素材層の他側面に沿い貼着してなるポリエステル系樹脂製の長手状他側分離層とでもって形成したなる粘着素材ロールを予め準備して、
前記保護フィルムロールを前記加飾フィルム部材ロールに沿い貼着してフィルム貼着ロール体を形成する第1工程と、
前記フィルム貼着ロール体を前記遊技基板に対応する長さにて切断して保護フィルム及び加飾フィルム部材からなる貼着フィルム層として形成する第2工程と、
前記貼着フィルム層の前記加飾フィルム部材の前記保護フィルムとは反対側の印刷面に所定の図柄を形成し、当該印刷面の一部に、ホログラム箔を付着させるための透明な特殊インクを印刷し、当該特殊インクの印刷された部分にホログラム箔を転写させて印刷貼着フィルム層として形成する第3工程と、
前記粘着素材ロールからその前記一側分離層を剥がしながら、当該粘着素材ロールの前記粘着素材層を前記印刷貼着フィルム層の前記加飾フィルム部材の前記印刷側面に沿い貼着して前記印刷貼着フィルム層にあわせて切断し粘着層とし、前記保護フィルム、前記加飾フィルム部材、前記粘着層及び前記他側分離層からなる複層貼着体として形成する第4工程と、
前記複層貼着体のうち前記遊技基板の前記開口部の内周面に対する対応部位を、前記保護フィルムを除き前記他側分離層から前記加飾フィルム部材にかけて切り込み、切り込み済み対応部位として形成する第5工程と、
前記切り込み済みの前記保護フィルム、前記加飾フィルム部材、前記粘着層及び前記他側分離層からなる切り込み済み複層貼着体を、前記他側分離層を剥がしながら、前記粘着層にて、前記遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第6工程と、
当該第6工程後、前記保護フィルムを前記加飾フィルム部材から剥がしながら、前記切り込み済み複層貼着体の加飾フィルム部材及び粘着層のうち前記切り込み済み対応部位の内側部位を前記保護フィルムと共に一体的に除去する第7工程とを備えて、
前記第1〜第7の工程を前記所定の雰囲気温度の環境内で行い、前記第7工程後所定の短時間内に前記化粧シートの異常或いは前記粘着層と前記遊技基板との間に異物の混入が発見されたとき、前記化粧シートを前記遊技基板から剥がして新たな化粧シートを前記遊技基板に前記第1〜第7の工程を経て貼着し直すことで製造するようにしたことを特徴とする遊技盤の製造方法。 In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As the gaming board, a gaming board made of transparent polycarbonate resin or transparent acrylic resin formed to have an opening necessary for assembling the effect display device of the various gaming parts is prepared in advance.
Prepare in advance a protective film roll made of a longitudinal film body made of a first thermoplastic resin and a decorative film member roll made of a longitudinal film body made of a transparent second thermoplastic resin,
Further, the adhesive material is made of a transparent adhesive that exhibits an adhesive property that is low immediately after the sticking when it is attached to the surface of the game board and increases with the passage of time in an environment of a predetermined atmosphere temperature. An adhesive material layer, a polyester resin-based longitudinally separated side layer that is adhered along one side of the adhesive material layer, and a polyester system that is adhered along the other side of the adhesive material layer Prepare in advance a pressure-sensitive adhesive material roll formed with a resinous longitudinal other side separation layer,
A first step of sticking the protective film roll along the decorative film member roll to form a film sticking roll body;
A second step of forming the film sticking roll as a sticking film layer comprising a protective film and a decorative film member by cutting the film sticking roll body at a length corresponding to the game board;
A predetermined special pattern is formed on the printing surface of the decorative film member on the opposite side of the protective film of the sticking film layer, and a transparent special ink for attaching a hologram foil to a part of the printing surface A third step of printing and transferring the hologram foil to the printed portion of the special ink to form a printed adhesive film layer; and
While peeling the one side separation layer from the adhesive material roll, the adhesive material layer of the adhesive material roll is adhered along the printing side surface of the decorative film member of the printing adhesive film layer, and the printing paste is applied. A fourth step of forming an adhesive layer by cutting according to the adhesive film layer, and forming as a multilayer adhesive body comprising the protective film, the decorative film member, the adhesive layer, and the other side separation layer;
A portion corresponding to the inner peripheral surface of the opening portion of the game board in the multilayer adhesive body is cut from the other side separation layer to the decorative film member except for the protective film, and formed as a cut corresponding portion. A fifth step;
In the adhesive layer, while peeling the other side separation layer, the cut multilayer adhesive body composed of the cut protective film, the decorative film member, the adhesive layer and the other side separation layer, A sixth step of adhering to the surface of the game board by pressing with a pressure within a predetermined pressure range;
After the said 6th process, while peeling off the said protective film from the said decorative film member, among the decorative film member and adhesive layer of the said cut | notched multilayer sticking body, the inner side part of the said cut corresponding | compatible part with the said protective film And a seventh step of removing integrally,
The first to seventh steps are performed in an environment of the predetermined ambient temperature, and after the seventh step, an abnormality of the decorative sheet or a foreign matter between the adhesive layer and the game board within a predetermined short time. When mixing is found, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to seventh steps and manufactured. A game board manufacturing method.
前記第5工程において、当該切り込みと併せて、ホログラム箔が転写された前記帯状の領域を含む領域を当該加飾フィルム部材から切断して、前記切り込み済み複層貼着体の外周面形状を前記遊技基板の外周面形状に合わせることを特徴とする請求項10または11に記載の遊技盤の製造方法。 In the third step, when printing a transparent special ink for attaching the hologram foil, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fifth step, in combination with the incision, the region including the band-like region to which the hologram foil has been transferred is cut from the decorative film member, and the outer peripheral surface shape of the cut multilayer adhesive body is 12. The method of manufacturing a game board according to claim 10, wherein the game board is adapted to the shape of the outer peripheral surface of the game board.
前記遊技基板として、前記各種遊技部品のうちの演出表示装置を組み付けるに要する開口部を有するように形成してなる透明性ポリカーボネート樹脂製或いは透明性アクリル樹脂製の遊技基板を予め準備し、
第1熱可塑性樹脂製の長手状フィルム体からなる保護フィルムロール及び透明の第2熱可塑性樹脂製の長手状フィルム体からなる加飾フィルム部材ロールを予め準備し、
かつ、前記遊技基板の面に貼着されたとき当該貼着直後には低くその後の時間の経過に伴い高くなる粘着力特性を所定の雰囲気温度の環境にて発揮する透明性粘着剤を粘着素材とする粘着素材層と、当該粘着素材層の一側面に沿い貼着してなるポリエステル系樹脂製の長手状一側分離層と、前記粘着素材層の他側面に沿い貼着してなるポリエステル系樹脂製の長手状他側分離層とでもって形成したなる粘着素材ロールを予め準備して、
前記保護フィルムロールを前記加飾フィルム部材ロールに沿い貼着してフィルム貼着ロール体を形成する第1工程と、
前記フィルム貼着ロール体を前記遊技基板に対応する長さにて切断して保護フィルム及び加飾フィルム部材からなる貼着フィルム層として形成する第2工程と、
前記貼着フィルム層の前記加飾フィルム部材の前記保護フィルムとは反対側の印刷面に所定の図柄を形成し、当該印刷面の一部に、ホログラム箔を付着させるための透明な第1特殊インクを印刷し、当該第1特殊インクの印刷された部分にホログラム箔を転写させ、さらに、ホログラム箔が転写された部分とホログラム箔が転写されていない部分との間に生ずる段差を埋めてその表面をフラットにするために当該ホログラム箔が転写されていない部分に透明な第2特殊インクを印刷にて流し込んで印刷貼着フィルム層として形成する第3工程と、
前記粘着素材ロールからその前記一側分離層を剥がしながら、当該粘着素材ロールの前記粘着素材層を前記印刷貼着フィルム層の前記加飾フィルム部材の前記印刷側面に沿い貼着して前記印刷貼着フィルム層にあわせて切断し粘着層とし、前記保護フィルム、前記加飾フィルム部材、前記粘着層及び前記他側分離層からなる複層貼着体として形成する第4工程と、
前記複層貼着体のうち前記遊技基板の前記開口部の内周面に対する対応部位を、前記保護フィルムを除き前記他側分離層から前記加飾フィルム部材にかけて切り込み、切り込み済み対応部位として形成する第5工程と、
前記切り込み済みの前記保護フィルム、前記加飾フィルム部材、前記粘着層及び前記他側分離層からなる切り込み済み複層貼着体を、前記他側分離層を剥がしながら、前記粘着層にて、前記遊技基板の面に所定の圧力範囲以内の圧力による押圧でもって貼着する第6工程と、
当該第6工程後、前記保護フィルムを前記加飾フィルム部材から剥がしながら、前記切り込み済み複層貼着体の加飾フィルム部材及び粘着層のうち前記切り込み済み対応部位の内側部位を前記保護フィルムと共に一体的に除去する第7工程とを備えて、
前記第1〜第7の工程を前記所定の雰囲気温度の環境内で行い、前記第7工程後所定の短時間内に前記化粧シートの異常或いは前記粘着層と前記遊技基板との間に異物の混入が発見されたとき、前記化粧シートを前記遊技基板から剥がして新たな化粧シートを前記遊技基板に前記第1〜第7の工程を経て貼着し直すことで製造するようにしたことを特徴とする遊技盤の製造方法。 In a manufacturing method of a game board that is manufactured using a game board and a decorative sheet for assembling various game parts of a pachinko gaming machine,
As the gaming board, a gaming board made of transparent polycarbonate resin or transparent acrylic resin formed to have an opening necessary for assembling the effect display device of the various gaming parts is prepared in advance.
Prepare in advance a protective film roll made of a longitudinal film body made of a first thermoplastic resin and a decorative film member roll made of a longitudinal film body made of a transparent second thermoplastic resin,
Further, the adhesive material is made of a transparent adhesive that exhibits an adhesive property that is low immediately after the sticking when it is attached to the surface of the game board and increases with the passage of time in an environment of a predetermined atmosphere temperature. An adhesive material layer, a polyester resin-based longitudinally separated side layer that is adhered along one side of the adhesive material layer, and a polyester system that is adhered along the other side of the adhesive material layer Prepare in advance a pressure-sensitive adhesive material roll formed with a resinous longitudinal other side separation layer,
A first step of sticking the protective film roll along the decorative film member roll to form a film sticking roll body;
A second step of forming the film sticking roll as a sticking film layer comprising a protective film and a decorative film member by cutting the film sticking roll body at a length corresponding to the game board;
A transparent first special for forming a predetermined pattern on the printing surface of the decorative film member on the opposite side of the protective film of the sticking film layer and attaching a hologram foil to a part of the printing surface The ink is printed, and the hologram foil is transferred to the printed portion of the first special ink. Further, the step formed between the portion where the hologram foil is transferred and the portion where the hologram foil is not transferred is filled. A third step of forming a printed adhesive film layer by pouring a transparent second special ink into a portion where the hologram foil is not transferred in order to flatten the surface;
While peeling the one side separation layer from the adhesive material roll, the adhesive material layer of the adhesive material roll is adhered along the printing side surface of the decorative film member of the printing adhesive film layer, and the printing paste is applied. A fourth step of forming an adhesive layer by cutting according to the adhesive film layer, and forming as a multilayer adhesive body comprising the protective film, the decorative film member, the adhesive layer, and the other side separation layer;
A portion corresponding to the inner peripheral surface of the opening portion of the game board in the multilayer adhesive body is cut from the other side separation layer to the decorative film member except for the protective film, and formed as a cut corresponding portion. A fifth step;
In the adhesive layer, while peeling the other side separation layer, the cut multilayer adhesive body composed of the cut protective film, the decorative film member, the adhesive layer and the other side separation layer, A sixth step of adhering to the surface of the game board by pressing with a pressure within a predetermined pressure range;
After the said 6th process, while peeling off the said protective film from the said decorative film member, among the decorative film member and adhesive layer of the said cut | notched multilayer sticking body, the inner side part of the said cut corresponding | compatible part with the said protective film And a seventh step of removing integrally,
The first to seventh steps are performed in an environment of the predetermined ambient temperature, and after the seventh step, an abnormality of the decorative sheet or a foreign matter between the adhesive layer and the game board within a predetermined short time. When mixing is found, the decorative sheet is peeled off from the game board, and a new decorative sheet is attached to the game board through the first to seventh steps and manufactured. A game board manufacturing method.
前記第5工程において、当該切り込みと併せて、ホログラム箔が転写された前記帯状の領域を含む領域を当該加飾フィルム部材から切断して、前記切り込み済み複層貼着体の外周面形状を前記遊技基板の外周面形状に合わせることを特徴とする請求項13または14に記載の遊技盤の製造方法。 In the third step, when printing the first special ink, in order to stabilize the transfer of the hologram foil, a band-shaped region is printed along the outer periphery of the decorative film member,
In the fifth step, in combination with the incision, the region including the band-like region to which the hologram foil has been transferred is cut from the decorative film member, and the outer peripheral surface shape of the cut multilayer adhesive body is The method for manufacturing a game board according to claim 13 or 14, wherein the game board is adapted to the shape of the outer peripheral surface of the game board.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2015183314A JP2017055988A (en) | 2015-09-16 | 2015-09-16 | Game board and production method thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2015183314A JP2017055988A (en) | 2015-09-16 | 2015-09-16 | Game board and production method thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| JP2017055988A true JP2017055988A (en) | 2017-03-23 |
Family
ID=58388931
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2015183314A Pending JP2017055988A (en) | 2015-09-16 | 2015-09-16 | Game board and production method thereof |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP2017055988A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2019180670A (en) * | 2018-04-06 | 2019-10-24 | 株式会社シャリー商事 | Game board production method |
| JP2023049112A (en) * | 2021-09-29 | 2023-04-10 | 株式会社藤商事 | game machine |
-
2015
- 2015-09-16 JP JP2015183314A patent/JP2017055988A/en active Pending
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2019180670A (en) * | 2018-04-06 | 2019-10-24 | 株式会社シャリー商事 | Game board production method |
| JP7020678B2 (en) | 2018-04-06 | 2022-02-16 | 株式会社シャリー商事 | Manufacturing method of game board |
| JP2023049112A (en) * | 2021-09-29 | 2023-04-10 | 株式会社藤商事 | game machine |
| JP7462600B2 (en) | 2021-09-29 | 2024-04-05 | 株式会社藤商事 | Gaming Machines |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6384734B2 (en) | Method and apparatus for joining first film web and second film web | |
| JP6222172B2 (en) | label | |
| WO2008084332A3 (en) | Improvements to printing superimposed layers | |
| JPH06322328A (en) | Adhesive sheet material for labeling machine | |
| JPH02107682A (en) | Marking sheet | |
| CN109593484A (en) | Paster of surface anti sticking and the preparation method and application thereof | |
| KR101307134B1 (en) | Release film for transcribing pattern, transcription film for patterning and patterning method using the same | |
| JP6607739B2 (en) | Patch, laminate of patch, method of manufacturing patch, and method of manufacturing laminate of patch | |
| JP2020033529A (en) | Method for producing printed material | |
| JP2019180670A (en) | Game board production method | |
| JP2013210466A (en) | Label sheet and method of manufacturing article with print pattern | |
| JP6204804B2 (en) | Game board manufacturing method | |
| JP2021133650A (en) | Laminate | |
| CN111028661B (en) | Method for manufacturing blood label | |
| KR102858196B1 (en) | Adhesive layer-free parking sign member and manufacturing method thereof | |
| JP2023129835A (en) | Game board manufacturing method | |
| JP5750979B2 (en) | Elongated body with pattern structure layer and method for bonding pattern structure layer | |
| CN100559429C (en) | Adhesive label and adhesive label roll | |
| JP2002244561A (en) | Tire management label | |
| JP3164663U (en) | Label sheet | |
| KR101466636B1 (en) | Film work method utilizing pinacle and flat panel type pinacle | |
| KR102737819B1 (en) | Eco-friendly label, method and system for manufacturing thereof, and method and system for attaching thereof | |
| KR102377451B1 (en) | structure for inner sheet having non-bond sticker | |
| CN204614353U (en) | Self-adhesive tape with traction connection layer | |
| JP6388363B2 (en) | Sticking method for sticking a sticking machine and a sticking member to a sticking member |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| RD04 | Notification of resignation of power of attorney |
Free format text: JAPANESE INTERMEDIATE CODE: A7424 Effective date: 20180425 |