JP2012146889A - Method for grinding wafer - Google Patents
Method for grinding wafer Download PDFInfo
- Publication number
- JP2012146889A JP2012146889A JP2011005414A JP2011005414A JP2012146889A JP 2012146889 A JP2012146889 A JP 2012146889A JP 2011005414 A JP2011005414 A JP 2011005414A JP 2011005414 A JP2011005414 A JP 2011005414A JP 2012146889 A JP2012146889 A JP 2012146889A
- Authority
- JP
- Japan
- Prior art keywords
- wafer
- grinding
- thickness
- back surface
- annular convex
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images






Landscapes
- Mechanical Treatment Of Semiconductor (AREA)
Abstract
【課題】 所定深さの円形凹部と該円形凹部を囲繞する環状凸部を有するウエーハの研削方法を提供することである。
【解決手段】 ウエーハ裏面の中央部を研削砥石で第1の厚みまで研削して、該第1の厚みを有する円形凹部と該円形凹部を囲繞する環状凸部とを形成するウエーハの研削方法であって、ウエーハの直径の略1/2の直径を有する研削砥石でウエーハ裏面の少なくとも該環状凸部部分を含むウエーハの外周縁領域を該第1の厚みに所定値を加算した第2の厚みまで研削する第1研削ステップと、該第1研削ステップを実施した後、該研削砥石で該環状凸部部分を除くウエーハ裏面の中央部を該第1の厚みまで研削して底部に該第1の厚みを有する円形凹部と該円形凹部を囲繞する該第2の厚みからなる環状凸部とを形成する第2研削ステップと、を具備したことを特徴とする。
【選択図】図6PROBLEM TO BE SOLVED: To provide a method for grinding a wafer having a circular concave portion having a predetermined depth and an annular convex portion surrounding the circular concave portion.
A wafer grinding method in which a central portion of a back surface of a wafer is ground to a first thickness with a grinding wheel to form a circular concave portion having the first thickness and an annular convex portion surrounding the circular concave portion. A second thickness obtained by adding a predetermined value to the first thickness of the outer peripheral edge region of the wafer including at least the annular convex portion on the back surface of the wafer with a grinding wheel having a diameter approximately half the diameter of the wafer. After the first grinding step and the first grinding step are performed, the center portion of the back surface of the wafer excluding the annular convex portion is ground to the first thickness with the grinding wheel, and the first portion is formed on the bottom portion. And a second grinding step for forming an annular convex portion having the second thickness surrounding the circular concave portion.
[Selection] Figure 6
Description
本発明は、ウエーハの裏面を研削して所定深さの円形凹部と該円形凹部を囲繞する環状凸部とを形成するウエーハの研削方法に関する。 The present invention relates to a wafer grinding method in which a rear surface of a wafer is ground to form a circular concave portion having a predetermined depth and an annular convex portion surrounding the circular concave portion.
半導体デバイスの製造プロセスにおいては、略円盤形状である半導体ウエーハの表面に格子状に配列されたストリートと呼ばれる分割予定ラインによって複数の領域が区画され、この区画された領域にIC、LSI等のデバイスを形成する。 In a semiconductor device manufacturing process, a plurality of regions are partitioned by dividing lines called streets arranged in a lattice pattern on the surface of a semiconductor wafer having a substantially disk shape, and devices such as ICs and LSIs are divided into these partitioned regions. Form.
そして、半導体ウエーハをストリートに沿って切削装置で切断することにより、半導体ウエーハが個々の半導体デバイス(半導体チップ)に分割され、分割された半導体デバイスはパソコン、携帯電話等の各種電気機器に広く利用されている。 Then, the semiconductor wafer is cut into individual semiconductor devices (semiconductor chips) by cutting the semiconductor wafer along the streets, and the divided semiconductor devices are widely used in various electric devices such as personal computers and mobile phones. Has been.
分割されるウエーハは、ストリートに沿って切断する前に裏面を研削して所定の厚みに加工される。近年、電気機器の軽量化、小型化を達成するために、ウエーハの厚さをより薄く、例えば50μm程度にすることが要求されている。 The wafer to be divided is processed to a predetermined thickness by grinding the back surface before cutting along the street. In recent years, in order to achieve a reduction in weight and size of electrical equipment, it has been required to make the wafer thinner, for example, about 50 μm.
このように薄く形成されたウエーハは取り扱いが困難になり、搬送等において破損する恐れがある。そこで、ウエーハのデバイス領域に対応する裏面のみを研削して円形凹部を形成し、デバイス領域を囲繞する外周余剰領域に対応するウエーハの裏面に環状凸部(環状補強部)を形成する研削方法が特開2007−19461号公報で提案されている。 Such thin wafers are difficult to handle and may be damaged during transportation. Accordingly, there is a grinding method in which only the back surface corresponding to the device region of the wafer is ground to form a circular recess, and an annular convex portion (annular reinforcing portion) is formed on the back surface of the wafer corresponding to the outer peripheral surplus region surrounding the device region. This is proposed in Japanese Patent Laid-Open No. 2007-19461.
ウエーハのデバイス領域に対応する裏面のみを研削後、環状凸部を除去せずにそのまま表面側からダイシング(切削)する場合や、ウエーハの研削の際にウエーハの表面に貼着した保護テープを研削後に剥離する場合等では、研削されたウエーハの円形凹部に嵌合するとともに環状凸部の上面を下方から支える凸形状のチャックテーブルが使用される(例えば、特開2010−16146号公報参照)。 After grinding only the back surface corresponding to the device area of the wafer and then dicing (cutting) from the front side without removing the annular protrusion, or grinding the protective tape attached to the wafer surface during wafer grinding In the case of peeling later, a convex chuck table that fits into the circular concave portion of the ground wafer and supports the upper surface of the annular convex portion from below is used (for example, see JP 2010-16146 A).
このような凸形状のチャックテーブルは、保持するウエーハの円形凹部の深さに対応した凸部を有している。研削する前のウエーハの厚みには規格があり例えば700μm等の一定厚みであるが、円形凹部の厚み(円形凹部の研削仕上げ厚み)は製造するデバイス毎に異なるため、円形凹部の深さも製造するデバイス毎に異なることになる。 Such a convex chuck table has a convex portion corresponding to the depth of the circular concave portion of the wafer to be held. There is a standard for the thickness of the wafer before grinding, for example, a constant thickness such as 700 μm. However, since the thickness of the circular recess (the grinding finish thickness of the circular recess) varies depending on the device to be manufactured, the depth of the circular recess is also manufactured. It will be different for each device.
従って、一定の段差の凸部を有するチャックテーブルで異なる深さの円形凹部を有するウエーハを吸引保持すると、吸引保持が不完全になるか又は円形凹部と環状凸部との境界からウエーハが割れてしまうという問題がある。 Therefore, when a wafer having a circular recess having a different depth is sucked and held by a chuck table having a certain level of protrusion, suction holding becomes incomplete or the wafer breaks from the boundary between the circular recess and the annular protrusion. There is a problem of end.
一方、円形凹部の深さに応じた複数の凸形状チャックテーブルを準備して、切削時に円形凹部の深さに応じてチャックテーブルを交換する対策も考えられるが、管理が煩雑となるとともにコスト高になるという問題がある。 On the other hand, it is possible to prepare a plurality of convex chuck tables according to the depth of the circular recess and replace the chuck table according to the depth of the circular recess at the time of cutting, but the management becomes complicated and the cost is high. There is a problem of becoming.
本発明はこのような点に鑑みてなされたものであり、その目的とするところは、異なる厚みの円形凹部を有するウエーハを一台のチャックテーブルで確実に吸引保持することのできるウエーハの研削方法を提供することである。 The present invention has been made in view of the above points, and an object of the present invention is to provide a wafer grinding method capable of reliably sucking and holding a wafer having circular concave portions having different thicknesses by a single chuck table. Is to provide.
本発明によると、ウエーハ裏面の中央部を研削砥石で第1の厚みまで研削して、該第1の厚みを有する円形凹部と該円形凹部を囲繞する環状凸部とを形成するウエーハの研削方法であって、ウエーハの直径の略1/2の直径を有する研削砥石でウエーハ裏面の少なくとも該環状凸部部分を含むウエーハの外周縁領域を該第1の厚みに所定値を加算した第2の厚みまで研削する第1研削ステップと、該第1研削ステップを実施した後、該研削砥石で該環状凸部部分を除くウエーハ裏面の中央部を該第1の厚みまで研削して底部に該第1の厚みを有する円形凹部と該円形凹部を囲繞する該第2の厚みからなる環状凸部とを形成する第2研削ステップと、を具備したことを特徴とするウエーハの研削方法が提供される。 According to the present invention, a wafer grinding method for forming a circular concave portion having the first thickness and an annular convex portion surrounding the circular concave portion by grinding the central portion of the back surface of the wafer to a first thickness with a grinding wheel. A second grinding wheel having a diameter approximately equal to a half of the diameter of the wafer, the outer peripheral area of the wafer including at least the annular convex portion on the back surface of the wafer being added with a predetermined value to the first thickness. After performing the first grinding step for grinding to the thickness and the first grinding step, the grinding wheel is used to grind the center of the back surface of the wafer excluding the annular convex portion to the first thickness to the bottom. And a second grinding step for forming a circular concave portion having a thickness of 1 and an annular convex portion having the second thickness surrounding the circular concave portion, and a method for grinding a wafer is provided. .
代替実施形態として、第1研削ステップでは、研削砥石でウエーハの裏面全面を研削して第2の厚みへと薄化するようにしてもよい。 As an alternative embodiment, in the first grinding step, the entire back surface of the wafer may be ground with a grinding wheel and thinned to the second thickness.
本発明によると、ウエーハの円形凹部は所定深さに形成されるため、一台の凸形状チャックテーブルで異なる厚さの円形凹部を有するウエーハを確実に吸引保持することができ、異なる段差(高さ)を有する複数の凸形状チャックテーブルを準備することは不必要となる。また、第1研削ステップで環状凸部の薄化も行うため、別途環状凸部の薄化用に他の研削ホイールを備えた研削装置が不必要となる。 According to the present invention, since the circular concave portion of the wafer is formed at a predetermined depth, a wafer having circular concave portions having different thicknesses can be reliably sucked and held by one convex chuck table, and different steps (high It is unnecessary to prepare a plurality of convex chuck tables with Further, since the annular convex portion is also thinned in the first grinding step, a grinding apparatus provided with another grinding wheel for thinning the annular convex portion becomes unnecessary.
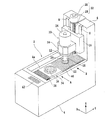
以下、図面を参照して本発明の実施形態を詳細に説明する。図1を参照すると、本発明のウエーハの研削方法を実施するのに適した研削装置2の斜視図が示されている。4は研削装置2のハウジング(ベース)であり、ハウジング4の後方にはコラム6が立設されている。コラム6には、上下方向にのびる一対のガイドレール8が固定されている。
Hereinafter, embodiments of the present invention will be described in detail with reference to the drawings. Referring to FIG. 1, there is shown a perspective view of a
この一対のガイドレール8に沿って研削ユニット(研削手段)10が上下方向に移動可能に装着されている。研削ユニット10は、ハウジング12と、ハウジング12を保持する支持部14を有しており、支持部14が一対のガイドレール8に沿って上下方向に移動される移動基台16に取り付けられている。
A grinding unit (grinding means) 10 is mounted along the pair of
研削ユニット10は、ハウジング12中に回転可能に収容されたスピンドル18と、スピンドル18の先端に固定されたマウンタ20と、マウンタ20にねじ締結され環状に配設された複数の研削砥石24(図4参照)を有する研削ホイール22と、スピンドル18を回転駆動するサーボモータ26を含んでいる。
The
研削装置2は、研削ユニット10を一対の案内レール8に沿って上下方向に移動するボールねじ28とパルスモータ30とから構成される研削ユニット送り機構32を備えている。パルスモータ30を駆動すると、ボールねじ28が回転し、移動基台16が上下方向に移動される。
The
ハウジング4の上面には凹部4aが形成されており、この凹部4aにチャックテーブル機構34が配設されている。チャックテーブル機構34はチャックテーブル36を有し、図示しない移動機構により図1に示されたウエーハ着脱位置Aと、研削ユニット10に対向する研削位置Bとの間でY軸方向に移動される。38,40は蛇腹である。ハウジング4の前方側には、研削装置2のオペレータが研削条件等を入力する操作パネル42が配設されている。
A
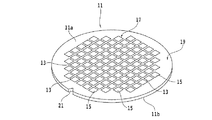
図2を参照すると、研削装置2でその裏面が研削される半導体ウエーハ11の表面側斜視図が示されている。半導体ウエーハ11は、例えば厚さが700μmのシリコンウエーハからなっており、表面11aに複数のストリート13が格子状に形成されているとともに、該複数のストリート13によって区画された複数の領域にIC、LSI等のデバイス15が形成されている。
Referring to FIG. 2, a front side perspective view of a
このように構成された半導体ウエーハ11は、デバイス15が形成されているデバイス領域17と、デバイス領域17を囲繞する外周余剰領域19を備えている。また、半導体ウエーハ11の外周には、シリコンウエーハの結晶方位を示すマークとしてのノッチ21が形成されている。
The
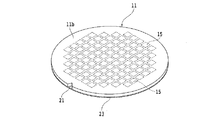
半導体ウエーハ11の表面11aには、保護テープ貼着工程により保護テープ23が貼着される。従って、半導体ウエーハ11の表面11aは保護テープ23によって保護され、図3に示すように、裏面11bが露出する状態となり、裏面11bを上側にして研削装置2のチャックテーブル36に吸引保持される。
A
以下、図4乃至図11を参照して、本発明の研削方法について詳細に説明する。図4を参照すると、本発明研削方法の第1研削ステップの第1実施形態を示す斜視図が示されている。図5はその説明図である。 Hereinafter, the grinding method of the present invention will be described in detail with reference to FIGS. Referring to FIG. 4, a perspective view showing a first embodiment of the first grinding step of the grinding method of the present invention is shown. FIG. 5 is an explanatory diagram thereof.
本発明の研削方法では、ウエーハ11の直径の略1/2の直径を有する研削ホイール22を使用する。よって、環状に配設された研削砥石24の直径もウエーハ11の直径の略1/2である。
In the grinding method of the present invention, a grinding
例えば、直径φ200mmのウエーハ11を研削する場合には、研削ホイール22の直径、即ち環状に配設された研削砥石24の直径が95〜99mmの範囲内であるのが好ましい。
For example, when grinding the
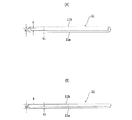
図6(A)は第1研削ステップを実施する前のウエーハ11の側面図を示しており、本発明の研削方法は、ウエーハ11のデバイス領域17に対応するウエーハ11の裏面を研削して第1の厚みt1を有する円形凹部と該円形凹部を囲繞する第2の厚みt2を有する環状凸部を形成する研削方法である。
FIG. 6A shows a side view of the
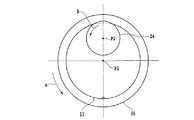
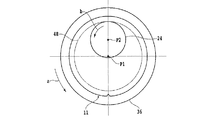
第1研削ステップでは、図4及び図5に示すように、チャックテーブル36でウエーハ11の保護テープ23側を吸引保持し、環状に配設された研削砥石24の一部がウエーハ11の外周から突出するように研削砥石24をウエーハ11の裏面11bに当接させる。図5でP1はチャックテーブル36の中心であり、P2は研削砥石24の中心である。
In the first grinding step, as shown in FIGS. 4 and 5, the
第1実施形態に係る第1研削ステップでは、チャックテーブル36をY軸方向には移動させない状態で矢印a方向に例えば300rpmで回転しつつ、研削ホイール22を矢印b方向に例えば6000rpmで回転させながら、切削ユニット送り機構32を駆動して、所定の研削送り速度でウエーハ11の外周余剰領域19に対応するウエーハ11の裏面11bを含んだ領域を研削する。
In the first grinding step according to the first embodiment, while the chuck table 36 is not moved in the Y-axis direction, the grinding
接触式又は非接触式の厚み測定ゲージにより研削部分のウエーハ11の厚みを測定しながら、図6に示すように、第1の厚みt1に所定値hを加算した第2の厚み測定器t2にまでウエーハ11を研削する。
As shown in FIG. 6, while measuring the thickness of the
本発明の第1研削ステップの第1実施形態では、研削砥石24はウエーハ11の中心部分には当接しないので、第1研削ステップ終了後のウエーハ11の裏面11bには、図6(B)に示すように、未研削領域である円形凹部25が残存する。
In the first embodiment of the first grinding step of the present invention, the grinding
この第1研削ステップは、図7の第2実施形態に示すように、チャックテーブル36をY軸方向に低速で移動させながら実施してもよい。この実施形態の第1研削ステップによると、チャックテーブル36をY軸方向に移動させる他は、上述した第1実施形態の第1研削ステップと同一条件で実施するため、第1研削ステップ終了後のウエーハ11は、図8(B)に示すように、第1の厚みt1に所定値hを加算した第2の厚みt2まで一様に研削される。
This first grinding step may be performed while moving the chuck table 36 in the Y-axis direction at a low speed, as shown in the second embodiment of FIG. According to the first grinding step of this embodiment, since the chuck table 36 is moved under the same conditions as the first grinding step of the first embodiment described above except that the chuck table 36 is moved in the Y-axis direction, As shown in FIG. 8B, the
本発明の研削方法では、上述した第1研削ステップを実施した後、第2研削ステップを実施する。この第2研削ステップでは、図10に最もよく示されるように、環状に配設された研削砥石24の外周がウエーハ11のデバイス領域17と外周余剰領域19の境界線48に接するとともに、チャックテーブル36の中心P1を通過するように設定される。
In the grinding method of the present invention, after the first grinding step described above is performed, the second grinding step is performed. In this second grinding step, as best shown in FIG. 10, the outer periphery of the
この状態で、チャックテーブル36を矢印aで示す方向に例えば300rpmで回転しつつ、研削砥石24を矢印bで示す方向に例えば6000rpmで回転させるとともに、切削ユニット送り機構32を駆動して、研削砥石24をウエーハ11の裏面11bに接触させる。そして、研削ホイール22を所定の研削送り速度で下方に所定量研削送りする。
In this state, while rotating the chuck table 36 in the direction indicated by the arrow a at 300 rpm, for example, the grinding
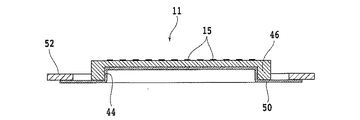
接触式又は非接触式の厚み測定ゲージでウエーハ11の厚みを測定しながらウエーハ11を第1の厚みt1、例えば30μmまで研削する。第2研削ステップが終了すると、図11に示すように、ウエーハ11の裏面11bに第1の厚みt1の円形凹部44が形成されるとともに、円形凹部44を囲繞する第2の厚みt2の環状凸部(環状補強部)46が形成される。
While measuring the thickness of the
第2の厚み測定t2は、第1の厚みt1に所定値hを加算した厚みであるため、円形凹部44の深さhは常に一定の所定値となり、環状凸部46の厚みt2は円形凹部44の研削量、即ち円形凹部46の厚みt1に応じて変化する。
Since the second thickness measurement t2 is a thickness obtained by adding a predetermined value h to the first thickness t1, the depth h of the
本発明の研削方法により研削されたウエーハ11は、ウエーハ11の切削加工に先立って、その外周部が環状フレーム52に装着されたダイシングテープ(粘着テープ)50に貼着される。ダイシングテープ50は、環状凸部46のみでなく円形凹部44にも回り込むように貼着される。
The
図13を参照すると、切削装置のチャックテーブル54の一例の縦断面図が示されている。チャックテーブル54は、真空吸引路58が形成された回転軸56と、回転軸56上の搭載固定された枠体60を具備している。枠体60はSUS等の金属から形成され、所定高さhの円形凸部62を有している。円形凸部62には装着用円形凹部64が形成され、円形凹部64中にはポーラスなセラミック等から形成された円板形状のポーラス吸着部68が配設されている。
Referring to FIG. 13, there is shown a longitudinal sectional view of an example of the chuck table 54 of the cutting apparatus. The chuck table 54 includes a
枠体60には装着用円形凹部64に連通する真空吸引路66が形成されており、真空吸引路66は回転軸52の真空吸引路58を介して図示しない真空吸引源に接続されている。
A
本発明の研削方法により研削されたウエーハ11は、所定深さhの円形凹部44と円形凹部44を囲繞する環状凸部46を有しているため、チャックテーブル54の円形凸部62にウエーハ11の円形凹部44を嵌合するようにウエーハ11をチャックテーブル54上に搭載すると、円形凹部44がチャックテーブル54のポーラス吸着部68により支持され、環状凸部46が枠体60により支持される。よって、ポーラス吸着部68を真空吸引源に接続することにより、ウエーハ11を確実に吸引保持することができる。
The
2 研削装置
10 研削手段(研削ユニット)
11 半導体ウエーハ
13 ストリート
15 デバイス
17 デバイス領域
19 外周余剰領域
22 研削ホイール
24 研削砥石
36 チャックテーブル
t1 第1の厚み
t2 第2の厚み
h 所定値(円形凹部の深さ)
44 円形凹部
46 環状凸部
2 Grinding
DESCRIPTION OF
44
Claims (2)
ウエーハの直径の略1/2の直径を有する研削砥石でウエーハ裏面の少なくとも該環状凸部部分を含むウエーハの外周縁領域を該第1の厚みに所定値を加算した第2の厚みまで研削する第1研削ステップと、
該第1研削ステップを実施した後、該研削砥石で該環状凸部部分を除くウエーハ裏面の中央部を該第1の厚みまで研削して底部に該第1の厚みを有する円形凹部と該円形凹部を囲繞する該第2の厚みからなる環状凸部とを形成する第2研削ステップと、
を具備したことを特徴とするウエーハの研削方法。 A method of grinding a wafer by grinding a central portion of a back surface of a wafer to a first thickness with a grinding wheel to form a circular concave portion having the first thickness and an annular convex portion surrounding the circular concave portion,
The outer peripheral edge region of the wafer including at least the annular convex portion on the back surface of the wafer is ground to a second thickness obtained by adding a predetermined value to the first thickness with a grinding wheel having a diameter approximately half the diameter of the wafer. A first grinding step;
After carrying out the first grinding step, the central portion of the wafer back surface except the annular convex portion is ground to the first thickness with the grinding wheel and the circular concave portion having the first thickness at the bottom and the circular shape A second grinding step for forming an annular convex portion having the second thickness surrounding the concave portion;
A method for grinding a wafer, comprising:
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011005414A JP2012146889A (en) | 2011-01-14 | 2011-01-14 | Method for grinding wafer |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011005414A JP2012146889A (en) | 2011-01-14 | 2011-01-14 | Method for grinding wafer |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| JP2012146889A true JP2012146889A (en) | 2012-08-02 |
Family
ID=46790146
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2011005414A Pending JP2012146889A (en) | 2011-01-14 | 2011-01-14 | Method for grinding wafer |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP2012146889A (en) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPWO2016056124A1 (en) * | 2014-10-10 | 2017-04-27 | 三菱電機株式会社 | Manufacturing method of semiconductor device |
| JP2017157750A (en) * | 2016-03-03 | 2017-09-07 | 株式会社ディスコ | Processing method of wafer |
| US9966293B2 (en) | 2014-09-19 | 2018-05-08 | Infineon Technologies Ag | Wafer arrangement and method for processing a wafer |
| JP2018069348A (en) * | 2016-10-25 | 2018-05-10 | 株式会社ディスコ | How to shape the chuck table |
| KR20190111761A (en) | 2018-03-22 | 2019-10-02 | 도요타 지도샤(주) | Wafer grinding method |
| CN115533625A (en) * | 2022-09-26 | 2022-12-30 | 杭州富芯半导体有限公司 | A Taiko Wafer Grinding Process |
| US11626371B2 (en) | 2020-12-28 | 2023-04-11 | Infineon Technologies Ag | Semiconductor structure with one or more support structures |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007173487A (en) * | 2005-12-21 | 2007-07-05 | Disco Abrasive Syst Ltd | Wafer processing method and apparatus |
| JP2009141276A (en) * | 2007-12-10 | 2009-06-25 | Fuji Electric Device Technology Co Ltd | Semiconductor device and manufacturing method thereof |
-
2011
- 2011-01-14 JP JP2011005414A patent/JP2012146889A/en active Pending
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007173487A (en) * | 2005-12-21 | 2007-07-05 | Disco Abrasive Syst Ltd | Wafer processing method and apparatus |
| JP2009141276A (en) * | 2007-12-10 | 2009-06-25 | Fuji Electric Device Technology Co Ltd | Semiconductor device and manufacturing method thereof |
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US9966293B2 (en) | 2014-09-19 | 2018-05-08 | Infineon Technologies Ag | Wafer arrangement and method for processing a wafer |
| JPWO2016056124A1 (en) * | 2014-10-10 | 2017-04-27 | 三菱電機株式会社 | Manufacturing method of semiconductor device |
| US10134598B2 (en) | 2014-10-10 | 2018-11-20 | Mitsubishi Electric Corporation | Method for manufacturing semiconductor device |
| DE112014007049B4 (en) | 2014-10-10 | 2024-08-22 | Rohm Co., Ltd. | Method for manufacturing a semiconductor device |
| JP2017157750A (en) * | 2016-03-03 | 2017-09-07 | 株式会社ディスコ | Processing method of wafer |
| JP2018069348A (en) * | 2016-10-25 | 2018-05-10 | 株式会社ディスコ | How to shape the chuck table |
| KR20190111761A (en) | 2018-03-22 | 2019-10-02 | 도요타 지도샤(주) | Wafer grinding method |
| US11491610B2 (en) | 2018-03-22 | 2022-11-08 | Disco Corporation | Wafer grinding method |
| DE102019203894B4 (en) | 2018-03-22 | 2024-05-08 | Denso Corporation | Wafer grinding process |
| US11626371B2 (en) | 2020-12-28 | 2023-04-11 | Infineon Technologies Ag | Semiconductor structure with one or more support structures |
| CN115533625A (en) * | 2022-09-26 | 2022-12-30 | 杭州富芯半导体有限公司 | A Taiko Wafer Grinding Process |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103084950B (en) | Wafer processing method | |
| JP5877663B2 (en) | Wafer grinding method | |
| JP5500942B2 (en) | Wafer processing method | |
| JP2010186971A (en) | Wafer processing method | |
| JP2011124266A (en) | Method of processing wafer | |
| JP2009004406A (en) | Substrate processing method | |
| JP2012043825A (en) | Wafer processing method | |
| JP2009125915A (en) | Grinding wheel mounting mechanism | |
| JP2019012773A (en) | Processing method of wafer | |
| JP2010016146A (en) | Chuck table of processing apparatus | |
| JP5121390B2 (en) | Wafer processing method | |
| JP2010247311A (en) | Workpiece grinding method | |
| JP2011131291A (en) | Grinder and method of grinding wafer using the same | |
| JP5101267B2 (en) | Wafer processing method | |
| JP5700988B2 (en) | Wafer grinding method | |
| JP2010093005A (en) | Processing method of wafer | |
| JP2010094789A (en) | Grinding wheel | |
| JP2010021330A (en) | Method of processing wafer | |
| JP2012231057A (en) | Method for processing wafer | |
| JP2011071287A (en) | Method of processing wafer | |
| JP2011071289A (en) | Method of processing wafer | |
| JP2012043824A (en) | Wafer processing method and protection member | |
| JP5473684B2 (en) | Wafer processing method | |
| JP2011071288A (en) | Method of processing wafer | |
| JP6195484B2 (en) | Wafer processing method |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20131213 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20141107 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20141118 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20150116 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20150609 |
|
| A02 | Decision of refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A02 Effective date: 20151225 |