JP2009164381A - Bulk feeder - Google Patents
Bulk feeder Download PDFInfo
- Publication number
- JP2009164381A JP2009164381A JP2008001239A JP2008001239A JP2009164381A JP 2009164381 A JP2009164381 A JP 2009164381A JP 2008001239 A JP2008001239 A JP 2008001239A JP 2008001239 A JP2008001239 A JP 2008001239A JP 2009164381 A JP2009164381 A JP 2009164381A
- Authority
- JP
- Japan
- Prior art keywords
- dimensional
- electronic component
- passage
- height
- width
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 230000003287 optical effect Effects 0.000 claims description 8
- 239000000428 dust Substances 0.000 abstract description 12
- 230000000694 effects Effects 0.000 description 9
- 238000002347 injection Methods 0.000 description 8
- 239000007924 injection Substances 0.000 description 8
- 230000009471 action Effects 0.000 description 7
- 238000000034 method Methods 0.000 description 7
- 239000011800 void material Substances 0.000 description 7
- 238000007664 blowing Methods 0.000 description 6
- 230000008569 process Effects 0.000 description 6
- 230000007246 mechanism Effects 0.000 description 4
- 230000002093 peripheral effect Effects 0.000 description 4
- 230000002950 deficient Effects 0.000 description 3
- 230000008030 elimination Effects 0.000 description 3
- 238000003379 elimination reaction Methods 0.000 description 3
- 238000013019 agitation Methods 0.000 description 2
- 230000008859 change Effects 0.000 description 2
- 238000006073 displacement reaction Methods 0.000 description 2
- 238000003756 stirring Methods 0.000 description 2
- 239000003990 capacitor Substances 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000002474 experimental method Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
Images




Landscapes
- Chutes (AREA)
- Attitude Control For Articles On Conveyors (AREA)
- Supply And Installment Of Electrical Components (AREA)
Abstract
Description
本発明は、バラ状態で収納されている電子部品を所定向きに整列して供給するバルクフィーダに関する。 The present invention relates to a bulk feeder that supplies electronic components stored in a loose state in an aligned manner.
この種のバルクフィーダには、長さ>幅=高さの寸法関係或いは長さ>幅>高さの寸法関係を有する直方体形状の電子部品をバラ状態で収納するための3次元室と、該3次元室内の電子部品を幅及び高さの向きが揃った姿勢で取り込むための2次元室と、該2次元室内の電子部品を幅,高さ及び長さの向きが揃った姿勢で取り込んで自重移動させるための横断面矩形の1次元通路と、を備えたものが存在する。 A bulk feeder of this type includes a three-dimensional chamber for storing a rectangular parallelepiped electronic component having a length> width = height dimensional relationship or length> width> height dimensional relationship; A two-dimensional room for taking electronic components in a three-dimensional room in a posture in which the width and height are aligned, and an electronic component in the two-dimensional room in a posture in which the directions of width, height, and length are aligned. There is a one-dimensional passage having a rectangular cross section for moving by its own weight.
3次元室は電子部品をその姿勢を制限すること無しに収納できる形状を成していて、3次元室内に収納された電子部品は該3次元室内をランダムな姿勢で自由に移動することができる。2次元室は電子部品の幅の最大寸法(=基準幅+公差)或いは高さの最大寸法(=基準高さ+公差)よりも僅かに大きな間隔を有する平行スペースから成り、3次元室から2次元室内に取り込まれた電子部品は該2次元室内を幅及び高さの向きが揃った姿勢で移動することができる。1次元通路は電子部品の幅の最大寸法(=基準幅+公差)よりも僅かに大きな寸法の内面と高さの最大寸法(=基準高さ+公差)よりも僅かに大きな寸法の内面とが隣り合う横断面矩形の通路から成り、2次元室から1次元通路内に取り込まれた電子部品は該1次元通路内を幅,高さ及び長さの向きが揃った姿勢で自重により下方移動することができる。 The three-dimensional room has a shape that can store electronic parts without restricting the posture thereof, and the electronic parts housed in the three-dimensional room can move freely in the three-dimensional room in a random posture. . The two-dimensional chamber is composed of parallel spaces having a space slightly larger than the maximum width (= reference width + tolerance) or the maximum height (= reference height + tolerance) of the electronic component. The electronic component taken into the dimension room can move in the two-dimensional room in a posture in which the directions of width and height are aligned. The one-dimensional path has an inner surface slightly larger than the maximum width (= reference width + tolerance) of the electronic component and an inner surface slightly larger than the maximum height (= reference height + tolerance). An electronic component that is composed of a passage having a rectangular cross section adjacent to each other and taken into the one-dimensional passage from the two-dimensional chamber moves downward within the one-dimensional passage by its own weight in a posture in which the width, height, and length are aligned. be able to.
前記バルクフィーダは基本的には電子部品の姿勢を3次元→2次元→1次元の順に制御することによって所期の整列供給を行うものであるため、良品寸法の電子部品、即ち、長さと幅と高さのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる電子部品を用いることが肝要となる。
ところで、前記バルクフィーダの3次元室内には必要に応じて電子部品が補充されることから、補充の際に外部から3次元室内に入り込んだ塵埃や、補充の際或いはその前後で電子部品から剥がれ落ちた欠片等が、3次元室内に収納されている電子部品に付着する恐れがある。 By the way, electronic parts are replenished as necessary in the three-dimensional chamber of the bulk feeder, so that dust that has entered the three-dimensional room from the outside during replenishment, or peeled off from the electronic parts during or before replenishment. There is a possibility that dropped pieces or the like may adhere to electronic components housed in the three-dimensional room.
特に、1次元通路は電子部品が幅,高さ及び長さの向きが揃った姿勢で通過できる横断面形を有するものであるため、1次元通路内に取り込まれた電子部品に前記の塵埃や欠片等が付着していて幅と高さの少なくとも一方の外観上寸法が1次元通路を通過できない程度まで増していると、該電子部品が1次元通路を移動する過程で部品詰まりを生じて以後の供給が停止してしまうことがある。 In particular, since the one-dimensional passage has a cross-sectional shape through which the electronic component can pass in a posture in which the width, height, and length are aligned, the dust and the electronic component taken into the one-dimensional passage are If a chip or the like is attached and the external dimension of at least one of the width and height is increased to the extent that it cannot pass through the one-dimensional passage, the electronic component is clogged in the process of moving through the one-dimensional passage. Supply may stop.
この部品詰まりの発生頻度は電子部品1万個に対して1回発生するかしないかの度数ではあるが、該部品詰まりは1次元通路の様々な位置で生じるため、部品詰まりを生じたときには、まず、部品詰まりが生じている位置を探索し、その後に部品詰まりを解消する作業を施す必要を生じる。 The occurrence frequency of this component clogging is the frequency of whether or not it occurs once per 10,000 electronic components. However, since the component clogging occurs at various positions in the one-dimensional path, when the component clogging occurs, First, it is necessary to search for a position where the component is clogged and then perform an operation to eliminate the component clogging.
この位置探索及び詰まり解消の作業は意外に時間のかかる作業であり、その作業時間中は電子部品の供給が行えないわけであるから、バルクフィーダの稼働率が大きく低下することは勿論のこと、該バルクフィーダが設置されたマウンタ等の生産性にも大きな影響を生じてしまう。 This position search and clogging work is unexpectedly time-consuming work, and the electronic parts cannot be supplied during the work time. The productivity of a mounter or the like in which the bulk feeder is installed is also greatly affected.
本発明は前記事情に鑑みて創作されたもので、その目的とするところは、電子部品が1次元通路を移動する過程で部品詰まりを生じた場合でもこれを簡単に解消できるバルクフィーダを提供することにある。 The present invention was created in view of the above circumstances, and an object of the present invention is to provide a bulk feeder that can easily eliminate a component clogging in the process of moving an electronic component through a one-dimensional path. There is.
前記目的を達成するため、本発明は、長さ>幅=高さの寸法関係或いは長さ>幅>高さの寸法関係を有する直方体形状の電子部品をバラ状態で収納するための3次元室と、該3次元室内の電子部品を幅及び高さの向きが揃った姿勢で取り込むための2次元室と、該2次元室内の電子部品を幅,高さ及び長さの向きが揃った姿勢で取り込んで自重移動させるための横断面矩形の1次元通路とを備えたバルクフィーダであって、前記1次元通路の所定位置に設けられ、該1次元通路の横断面形を局部的に小さくした横断面形を有し、幅が基準幅+公差で高さが基準高さ+公差の電子部品の通過を許容する絞り部を備えている、ことをその特徴とする。 To achieve the above object, the present invention provides a three-dimensional chamber for storing a rectangular parallelepiped electronic component having a length> width = height dimension relationship or a length> width> height dimension relationship in a loose state. A two-dimensional chamber for taking the electronic components in the three-dimensional room in a posture in which the width and height are aligned, and a posture in which the electronic components in the two-dimensional chamber are aligned in the width, height, and length A one-dimensional passage having a rectangular cross-section for taking in and moving by its own weight, provided at a predetermined position of the one-dimensional passage, and locally reducing the cross-sectional shape of the one-dimensional passage It has a cross-sectional shape, and is characterized in that it has a throttle part that allows passage of electronic components whose width is a reference width + tolerance and whose height is a reference height + tolerance.
このバルクフィーダによれば、1次元通路の所定位置に該1次元通路の横断面形を局部的に小さくした横断面形を有し、且つ、幅Wが基準幅+公差で高さHが基準高さ+公差の電子部品の通過を許容する絞り部を設けてあるので、1次元通路内に取り込まれた電子部品に塵埃や欠片等が付着していて幅と高さの少なくとも一方の外観上寸法が絞り部を通過できない程度まで増している場合に該電子部品を1次元通路の絞り部の位置で積極的に詰まらせることができる。 According to this bulk feeder, a predetermined cross-sectional shape of the one-dimensional passage has a cross-sectional shape obtained by locally reducing the cross-sectional shape of the one-dimensional passage, and the width W is a reference width + tolerance and the height H is a reference. Since there is a throttle part that allows the passage of electronic components with height + tolerance, dust or debris adheres to the electronic components taken into the one-dimensional passage, and at least one of the width and height looks When the dimension is increased to such an extent that it cannot pass through the throttle part, the electronic component can be positively clogged at the position of the throttle part of the one-dimensional passage.
換言すれば、部品詰まりの原因となる電子部品が1次元通路内に取り込まれた場合でも該電子部品を常に同じ位置(絞り部の位置)で詰まらせることができるので、部品詰まりが生じている位置を探索する必要がないし、また、部品詰まりを生じる位置が定まっているので部品詰まりを解消する作業を迅速に行うことができる。従って、部品詰まりに伴う位置探索及び詰まり解消の作業を簡便化して、詰まり解消を極めて簡単に行うことができる。 In other words, even when an electronic component that causes component clogging is taken into the one-dimensional passage, the electronic component can always be clogged at the same position (the position of the throttle portion), so that component clogging occurs. There is no need to search for the position, and since the position where the component clogging occurs is fixed, the work for eliminating the component clogging can be performed quickly. Therefore, it is possible to simplify the position search and clogging work that accompanies clogging of the parts, and to clog clogging very easily.
本発明によれば、電子部品が1次元通路を移動する過程で部品詰まりを生じた場合でもこれを簡単に解消できるバルクフィーダを提供することができる。 According to the present invention, it is possible to provide a bulk feeder that can easily eliminate a component clogging in the process of moving an electronic component through a one-dimensional path.
本発明の前記目的とそれ以外の目的と、構成特徴と、作用効果は、以下の説明と添付図面によって明らかとなる。 The above object and other objects, structural features, and operational effects of the present invention will become apparent from the following description and the accompanying drawings.
[第1実施形態]
図1〜図6は本発明(バルクフィーダ)の第1実施形態を示す。
[First Embodiment]
1 to 6 show a first embodiment of the present invention (bulk feeder).
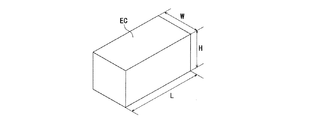
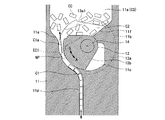
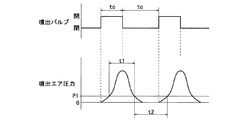
図1はバルクフィーダを取込ローターの第2ローターの厚さ方向中心で破断した縦断面図、図2(A)はバルクフィーダを図1のa−a線で破断した横断面図、図2(B)はバルクフィーダを図1のb−b線で破断した横断面図、図3は電子部品の拡大斜視図、図4(A)は図1に示した絞り部の拡大横断面図、図4(B)は図1に示した絞り部の拡大縦断面図、図5はバルクフィーダによる電子部品の整列供給動作の説明図、図6は噴出バルブの開閉タイミングと噴出エアの圧力との関係を示す図である。 FIG. 1 is a longitudinal sectional view of the bulk feeder taken in the thickness direction of the second rotor of the rotor, FIG. 2A is a transverse sectional view of the bulk feeder taken along the line aa in FIG. (B) is a cross-sectional view of the bulk feeder cut along line bb in FIG. 1, FIG. 3 is an enlarged perspective view of the electronic component, and FIG. 4 (A) is an enlarged cross-sectional view of the aperture shown in FIG. 4B is an enlarged vertical sectional view of the throttle portion shown in FIG. 1, FIG. 5 is an explanatory view of the operation of aligning and supplying electronic components by the bulk feeder, and FIG. 6 is a diagram showing the opening / closing timing of the ejection valve and the pressure of the ejection air. It is a figure which shows a relationship.
また、図1〜図6中の符号11はセンタープレート、12aは第1カバープレート、12bは第2カバープレート、13は取込ローター、14はローター軸、NPは絞り部、ECは電子部品である。
1 to 6,
まず、バルクフィーダのメカニズムを説明する前に、該バルクフィーダで用いられる電子部品ECについて図3を参照して説明する。 First, before explaining the mechanism of the bulk feeder, the electronic component EC used in the bulk feeder will be described with reference to FIG.
電子部品ECは、長さL(基準長さ±公差)>幅W(基準幅±公差)=高さH(基準高さ±公差)の寸法関係を有する直方体形状を成している。この電子部品ECは具体的にはコンデンサやインダクタや抵抗器等であって、表面の所定箇所に所定数の外部電極(図示省略)を有している。 The electronic component EC has a rectangular parallelepiped shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance) = height H (reference height ± tolerance). The electronic component EC is specifically a capacitor, inductor, resistor, or the like, and has a predetermined number of external electrodes (not shown) at predetermined positions on the surface.
次に、図1と図2(A)と図2(B)と図4(A)と図4(B)を参照してバルクフィーダのメカニズムについて説明する。ここでの説明では図1の手前を前、奥を後、左を左、右を右と表記する。 Next, the mechanism of the bulk feeder will be described with reference to FIGS. 1, 2A, 2B, 4A, and 4B. In this description, the front side of FIG. 1 is indicated as front, the back side as back, the left side as left, and the right side as right.
センタープレート11は、上部に後述の3次元室C3を構成するための空所11aを有し、該空所11aの下側に略180度の扇形状を成す空所11bを空所11aと連通して有し、該空所11bの前側に略90度の扇形状を成す空所11cを空所11aと連通して有し、該空所11cの下側に後述の1次元通路C1を構成するための矩形溝11dを有している。空所11bは後述の取込ローター13の第1ローター部13aの厚さよりも僅かに小さな深さを有し、第1ローター部13aをその上部が空所11aに露出した状態で回転自在に受容する。空所11cは後述の取込ローター13の第2ローター部13bの厚さよりも僅かに小さな深さを有し、第2ローター部13bをその上部が空所11aに露出した状態で回転自在に受容する
矩形溝11dは隣接する2つの内面の寸法が電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きく、該矩形溝11dの左内面は空所11bの外縁に沿って円弧状に上側に延びている。また、空所11aの下部左側には空所11aの左内面から矩形溝11dの左内面の延長端に至る湾曲したガイド面11eが設けられている。さらに、空所11aの下部右側には空所11aと空所11bとの境界を形成する傾斜したガイド面11fが設けられている。
The
取込ローター13は、全体が円盤状を成す第1ローター部13aと、第1ローター部13aと一体または別体に形成され、且つ、略60度の扇形状を成す第2ローター部13bとから成る。第2ローター部13bの略60度の円弧面の曲率中心と第1ローター部13aの環状外周面の曲率中心とは一致しており、両者の曲率中心部分にはローター軸14が取り付けられている。また、第1ローター部11aの上部には環状外周面の一部を切り欠いて形成された撹拌部13a1が設けられている。
The
第1ローター部13aの厚さは電子部品ECの長さの最大寸法(=基準長さ+公差)よりも大きく、第2ローター部13bの厚さは電子部品の幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きい。また、第2ローター部13bの略90度の円弧面の曲率半径は第1ロータ部13aの半径よりも小さく、第2ローター部13bの円弧面と第1ロータ部13aの環状外周面との段差は後述の1次元通路C1の上部湾曲部分の隣接する2つの内面を構成する。この段差により形成される2つの内面の寸法は、電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きい。
The thickness of the
この取込ローター13は、第2ローター部13bをセンタープレート11の空所11cに嵌め込み、且つ、第1ローター部13aを空所11bに嵌め込んだ後に、センタープレート11の前後面に第1,第2カバープレート12a,12bをネジ止め(ネジは図示省略)することによって、センタープレート11と第1,第2カバープレート12a,12bの内部に組み込まれている。この組み込みの際、ローター軸14の後側部分は第2カバープレート12bの軸支孔12b1に回転自在に挿入される。図示を省略したが、ローター軸14の第2カバープレート12bの後面から突出する部分にはローター軸14に所定の動作、即ち、取込ローター13を図1中でA方向に変位させ、且つ、変位後にB方向に変位させて復帰させる動作を付与するための駆動機構が接続されている。
The
また、センタープレート11を第1,第2カバープレート12a,12bで挟み込むことによって、センタープレート11の凹所11aは3次元室C3となり、取込ローター13の第1ローター部13の前面と第1カバープレート12aの後面との間の平行スペースは2次元室C2となり、センタープレート11の矩形溝11dと該矩形溝11dの上端と繋がる第2ローター部13bの円弧面と第1ロータ部13aの環状外周面との段差は1次元通路C1となる。
Further, by sandwiching the
要するに、3次元室C3は電子部品ECをその姿勢を制限すること無しに収納できる形状を成していて、3次元室C3内に収納された電子部品ECは該3次元室C3内をランダムな姿勢で自由に移動することができる。2次元室C2は電子部品ECの幅Wの最大寸法と高さHの最大寸法よりも僅かに大きな間隔を有する平行スペースから成り、3次元室C3から2次元室C2内に取り込まれた電子部品ECは該2次元室C2内を幅W及び高さHの向きが揃った姿勢で移動することができる。1次元通路C1は電子部品ECの幅Wの最大寸法よりも僅かに大きな内面と高さHの最大寸法よりも僅かに大きな内面とが隣り合う横断面矩形の通路から成り、2次元室C2から1次元通路C1内に取り込まれた電子部品ECは該1次元通路C1内を幅W,高さH及び長さの向きが揃った姿勢で自重により下方移動することができる。 In short, the three-dimensional chamber C3 has a shape that can store the electronic component EC without restricting the posture thereof, and the electronic component EC stored in the three-dimensional chamber C3 randomly enters the three-dimensional chamber C3. Can move freely in posture. The two-dimensional chamber C2 includes a parallel space having a space slightly larger than the maximum dimension of the width W and the maximum dimension of the height H of the electronic component EC, and the electronic component taken into the two-dimensional chamber C2 from the three-dimensional chamber C3. The EC can move in the two-dimensional chamber C2 in a posture in which the directions of the width W and the height H are aligned. The one-dimensional passage C1 is composed of a passage having a rectangular cross section in which an inner surface slightly larger than the maximum dimension of the width W of the electronic component EC and an inner surface slightly larger than the maximum dimension of the height H are adjacent to each other from the two-dimensional chamber C2. The electronic component EC taken into the one-dimensional passage C1 can move downward by its own weight in a posture in which the width W, height H, and length are aligned in the one-dimensional passage C1.
前記1次元通路C1は湾曲部分の上端をその入口C1aとしており、該入口C1aの下側(下流側)には、該1次元通路C1の横断面形を局部的に小さくした横断面形を有する絞り部NPが形成されている。この絞り部NPは、図4(A)及び図4(B)に示すように、前記1次元通路C1の隣接する2つの内面に設けられた縦断面台形の突起11g,12a1によって構成されており、図示例にあっては一方の突起11gはセンタープレート11に形成され、他方の突起12a1は第1カバープレート12aに形成されている。また、絞り部NPの横断面形は1次元通路C1の横断面形と相似の矩形であり、該絞り部NPの隣接する2つの内面の寸法WT1,WT2は電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きく設定されている。つまり、絞り部NPは幅が基準幅+公差で高さが基準高さ+公差の電子部品ECの通過を許容する。
The one-dimensional passage C1 has an upper end of a curved portion as an inlet C1a, and has a cross-sectional shape in which the cross-sectional shape of the one-dimensional passage C1 is locally reduced on the lower side (downstream side) of the inlet C1a. An aperture NP is formed. As shown in FIGS. 4 (A) and 4 (B), the narrowed portion NP is constituted by
また、図4(B)に示すように、前記1次元通路C1の絞り部NPの下側(下流側)には、1次元通路C1内にエアを噴出するためのエア噴出孔12a2が前記1次元通路C1と直交する向きで設けられている。図示例にあってはこのエア噴出孔12a2は前記1次元通路C1の1つの内面を構成する第1カバープレート12aに設けられている。このエア噴出孔12a2には、該エア噴出孔12a2からのエアの噴出を行うためのエア供給装置AFDがエア配管(符号無し)を介して接続されている。このエア供給装置AFDは、エアポンプAPと、エア噴出に係るエアの供給及び停止を制御する噴出バルブGVと、該噴出バルブGVを所定の開時間及び閉時間に基づいて間欠的に開閉し得るようにその動作を制御するコントローラCONとを備えている。
Further, as shown in FIG. 4B, an air ejection hole 12a2 for ejecting air into the one-dimensional passage C1 is provided on the lower side (downstream side) of the throttle portion NP of the one-dimensional passage C1. It is provided in a direction orthogonal to the dimension passage C1. In the illustrated example, the air ejection hole 12a2 is provided in the
次に、図5を参照してバルクフィーダによる電子部品ECの整列供給動作について説明する。 Next, the operation for aligning and supplying the electronic components EC by the bulk feeder will be described with reference to FIG.
バルクフィーダによる電子部品ECの整列供給動作は、良品寸法の電子部品EC、即ち、長さLと幅Wと高さHのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる電子部品ECを3次元室C3内にバラ状態で収納した後に、取込ローター13を図5中でA方向に所定角度変位させ、且つ、変位後にB方向に同一角度変位させて復帰させる動作を連続的或いは間欠的に行うと共に、エア噴出孔12a2(図4(B)参照)から1次元通路C1内に間欠的にエアを噴出する動作を行うことによって実行される。
The operation of aligning and supplying the electronic components EC by the bulk feeder is a non-defective electronic component EC, that is, the length L, the width W, and the height H are the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance. 5 is stored in a three-dimensional chamber C3 in a loose state, the take-in
取込ローター13の前記動作によって、3次元室C3内に収納されている電子部品ECは該3次元室C3から2次元室C2内に幅W及び高さHの向きが揃った姿勢で取り込まれる。取込ローター13の第1ローター部13aの上部は3次元室C3内に露出しているため、3次元室C3内に収納されている電子部品ECは第1ローター部13aの上部、主に撹拌部13a1による撹拌によってその幅W及び高さHの向きを変化して2次元室C2内に取り込まれるような作用を生じる。
By the operation of the take-in
また、取込ローター13の前記動作によって、2次元室C2内に取り込まれた電子部品ECは該2次元室C2から1次元通路C1内に幅W,高さH及び長さの向きが揃った姿勢で取り込まれる。取込ローター13の第2ローター部13bの上面は2次元室C2の底部に位置するため、2次元室C2内に取り込まれた電子部品ECは第2ローター部13bの上面の角度変化によってその長さLの向きを変化して1次元通路C1内に取り込まれるような作用を生じる。
Further, the electronic component EC taken into the two-dimensional chamber C2 by the operation of the taking-in
1次元通路C1内に取り込まれた電子部品ECは幅W,高さH及び長さLの向きが揃った姿勢で該1次元通路C1内を自重により下方移動する。1次元通路C1の入口C1aの下側(下流側)には絞り部NPが存在するが、1次元通路C1内に取り込まれた電子部品ECの幅W,高さH及び長さLのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる場合、該電子部品ECは絞り部NPを通過する。 The electronic component EC taken into the one-dimensional passage C1 moves downward in the one-dimensional passage C1 by its own weight in a posture in which the directions of the width W, the height H, and the length L are aligned. The throttle NP is present below (downstream) the inlet C1a of the one-dimensional passage C1, but the width W, height H, and length L of the electronic component EC taken into the one-dimensional passage C1 are respectively determined. When the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance are satisfied, the electronic component EC passes through the aperture NP.
バルクフィーダの3次元室C3内には必要に応じて電子部品ECが補充されることから、補充の際に外部から3次元室C3内に入り込んだ塵埃や、補充の際或いはその前後で電子部品ECから剥がれ落ちた欠片等が、3次元室C3内に収納されている電子部品ECに付着する恐れがある。依って、前述の整列供給動作によって1次元通路C1内に取り込まれた電子部品ECに前記の塵埃や欠片等が付着していて幅Wと高さHの少なくとも一方の外観上寸法が絞り部NPを通過できない程度まで増していると、該電子部品ECは1次元通路C1を移動する過程で絞り部NPで詰まって停止する。 Since the electronic component EC is replenished in the three-dimensional chamber C3 of the bulk feeder as necessary, the dust that has entered the three-dimensional chamber C3 from the outside during the replenishment, and the electronic component at the time of replenishment, or before and after that. There is a possibility that a piece or the like peeled off from the EC adheres to the electronic component EC stored in the three-dimensional chamber C3. Therefore, the dust, chips, and the like are attached to the electronic component EC taken into the one-dimensional passage C1 by the above-described alignment supply operation, and at least one of the external dimensions of the width W and the height H is the narrowed portion NP. If it has increased to such an extent that it cannot pass through the electronic component EC, the electronic component EC is clogged with the throttle NP and stopped in the process of moving through the one-dimensional passage C1.
前述の整列供給動作に併せてエア噴出孔12a2から1次元通路C1内に間欠的に噴出されるエアは、1次元通路C1内に取り込まれた電子部品ECが絞り部NPで詰まって停止したときに、該電子部品EC1(破線参照)を絞り部NPから上方に吹き上げて詰まりを解消する作用を発揮する。エアを間欠的に噴出する理由は非噴出時間を利用して前記の整列供給動作を支障なく行うことにあり、以下この点について図6を参照して説明する。 The air intermittently ejected from the air ejection holes 12a2 into the one-dimensional passage C1 in conjunction with the above-described alignment supply operation is stopped when the electronic component EC taken into the one-dimensional passage C1 is clogged with the throttle NP. In addition, the electronic component EC1 (see the broken line) is blown upward from the narrowed portion NP to exert an action of eliminating clogging. The reason why the air is intermittently ejected is to perform the alignment supplying operation without any trouble by using the non-ejection time, and this point will be described below with reference to FIG.
図6の符号toとtcは図4(B)に示したエア供給装置AFDの噴出バルブGVの開時間と閉時間を示すもので、該噴出バルブGVは所定の開時間to及び閉時間tcに基づいて間欠的に開閉し得るようにその動作をコントローラCONによって制御されている。図6から分かるようにエア噴出孔12a2から1次元通路C1内に噴出される実際上のエアの圧力は、前記噴出バルブGVの開時間toの開始点から徐々に増加してピークに達し該開時間toの終了点或いはその後から徐々に減少するような変化を示す。 Symbols to and tc in FIG. 6 indicate the opening time and closing time of the ejection valve GV of the air supply device AFD shown in FIG. 4B, and the ejection valve GV is at a predetermined opening time to and closing time tc. The operation is controlled by the controller CON so that it can be opened and closed intermittently. As can be seen from FIG. 6, the pressure of the actual air ejected from the air ejection hole 12a2 into the one-dimensional passage C1 gradually increases from the starting point of the opening time to of the ejection valve GV and reaches a peak. It shows a change that gradually decreases from the end point of time to or thereafter.
絞り部NPで詰まった電子部品ECを該絞り部NPから上方に吹き上げるには該電子部品ECのサイズ等に応じた所定値以上の圧力を必要とする。この圧力値をP1とするとエアの圧力が圧力値P1以上の区間t1が絞り部NPで詰まった電子部品ECを上方に吹き上げることが可能な時間(以下、吹き上げ時間t1と言う)となり、エアの圧力が圧力値p1未満の区間t2は吹き上げられた電子部品ECが自重落下することが可能な時間(以下、自重落下時間t2)となる。 In order to blow up the electronic component EC clogged with the throttle NP upward from the throttle NP, a pressure of a predetermined value or more according to the size of the electronic component EC or the like is required. When this pressure value is P1, it becomes the time during which the electronic component EC clogged with the throttle portion NP can be blown upward in the section t1 where the air pressure is equal to or higher than the pressure value P1 (hereinafter referred to as blow-up time t1). A section t2 where the pressure is less than the pressure value p1 is a time during which the blown-up electronic component EC can drop by its own weight (hereinafter referred to as “self-weight falling time t2”).
前記吹き上げ時間t1は圧力値P1以上の区間であるので、最低限の時間が確保されていれば絞り部NPで詰まった電子部品ECを該絞り部NPから上方に吹き上げて詰まりを解消することは可能である。しかし、絞り部NPで詰まった電子部品ECと共に吹き上げられた他の電子部品ECが元の高さ位置に落下する前に次の吹き上げが開始されてしまうと前述の整列供給動作は行えなくなってしまう。換言すれば、前述の整列供給動作は絞り部NPで詰まった電子部品ECと共に吹き上げられた他の電子部品ECが元の高さ位置に落下した後に行われることになるため、前記自重落下時間t2として十分な時間が確保できるように前記噴出バルブGVの閉時間tcを設定する必要がある。 Since the blow-up time t1 is a section equal to or greater than the pressure value P1, if the minimum time is secured, the electronic component EC clogged with the throttle NP is blown upward from the throttle NP to eliminate the clogging. Is possible. However, if the next blowing is started before the other electronic component EC blown up together with the electronic component EC clogged by the narrowed portion NP falls to the original height position, the above-described alignment supply operation cannot be performed. . In other words, the above-described alignment supply operation is performed after the other electronic component EC blown up together with the electronic component EC clogged by the narrowed portion NP falls to the original height position, and thus the dead weight falling time t2 It is necessary to set the closing time tc of the ejection valve GV so that a sufficient time can be secured.
例えば、前記開時間toを0.01秒としたときの前記吹き上げ時間t1が0.02秒で該吹き上げ時間t1において絞り部NPで詰まった電子部品ECを10mm吹き上げることができるときに、該電子部品ECと共に吹き上げられた他の電子部品ECが元の高さ位置に落下する時間が0.03秒の場合には、0.03秒を十分に超える時間を前記自重落下時間t2として得るために前記閉時間tcとして0.04秒以上をその値として採用する。 For example, when the blowing time t1 when the opening time to is 0.01 seconds is 0.02 seconds and the electronic component EC clogged with the throttle NP can be blown by 10 mm at the blowing time t1, When the time for another electronic component EC blown up with the component EC to drop to the original height position is 0.03 seconds, in order to obtain a time sufficiently exceeding 0.03 seconds as the dead weight falling time t2. The closing time tc is 0.04 seconds or more.
前記噴出バルブGVの開時間to及び閉時間tcは使用する電子部品ECのサイズ及び重量や絞り部NPで詰まった電子部品ECの上側に存する電子部品ECの数等によって異なるため、該開時間to及び閉時間tcは事前実験等によって適正な数値を選定する方法によって定めることが望ましい。 Since the opening time to and the closing time tc of the ejection valve GV vary depending on the size and weight of the electronic component EC to be used, the number of electronic components EC existing above the electronic component EC clogged with the throttle portion NP, etc., the opening time to The closing time tc is preferably determined by a method of selecting an appropriate numerical value by a preliminary experiment or the like.
このように、前述のバルクフィーダによれば、前記1次元通路C1の入口C1aの下側(下流側)に該1次元通路C1の横断面形を局部的に小さくした横断面形を有し、且つ、幅Wが基準幅+公差で高さHが基準高さ+公差の電子部品の通過を許容する絞り部NPを設けてあるので、1次元通路C1内に取り込まれた電子部品ECに塵埃や欠片等が付着していて幅Wと高さHの少なくとも一方の外観上寸法が絞り部NPを通過できない程度まで増している場合に該電子部品ECを1次元通路C1の絞り部NPの位置で積極的に詰まらせることができる。 Thus, according to the above-mentioned bulk feeder, it has a cross-sectional shape in which the cross-sectional shape of the one-dimensional passage C1 is locally reduced on the lower side (downstream side) of the inlet C1a of the one-dimensional passage C1. In addition, since the narrowed portion NP that allows passage of the electronic component having the width W of the reference width + tolerance and the height H of the reference height + tolerance is provided, the electronic component EC taken into the one-dimensional passage C1 has dust. If the electronic component EC is increased to such an extent that at least one of the width W and the height H cannot be passed through the throttle NP, the electronic component EC is positioned at the throttle NP of the one-dimensional passage C1. Can be actively clogged with.
換言すれば、部品詰まりの原因となる電子部品ECが1次元通路C1内に取り込まれた場合でも該電子部品ECを常に同じ位置(絞り部NPの位置)で詰まらせることができるので、部品詰まりが生じている位置を探索する必要がないし、また、部品詰まりを生じる位置が定まっているいるので部品詰まりを解消する作業を迅速に行うことができる。従って、部品詰まりに伴う位置探索及び詰まり解消の作業を簡便化して、詰まり解消を極めて簡単に行うことができる。 In other words, even when the electronic component EC causing the component clogging is taken into the one-dimensional passage C1, the electronic component EC can always be clogged at the same position (the position of the narrowed portion NP). It is not necessary to search for the position where the clogging occurs, and the position where the clogging occurs is fixed, so that the work for eliminating the clogging can be quickly performed. Therefore, it is possible to simplify the position search and clogging work that accompanies clogging of the parts, and to clog clogging very easily.
また、前述のバルクフィーダによれば、前記1次元通路C1の絞り部NPの下側(下流側)に該1次元通路C1内にエアを噴出するためのエア噴出孔12a2を設けると共に、このエア噴出孔12a2に該エア噴出孔12a2からのエアの噴出を行うためのエア供給装置AFDを接続してあるので、1次元通路C1内に取り込まれた電子部品ECが絞り部NPで詰まった場合でも、エア噴出孔12a2から1次元通路C1内に噴出されるエアによって絞り部NPで詰まった電子部品ECを該絞り部NPから上方に吹き上げて詰まりを解消することができる。 Further, according to the above-described bulk feeder, the air ejection hole 12a2 for ejecting air into the one-dimensional passage C1 is provided on the lower side (downstream side) of the throttle portion NP of the one-dimensional passage C1, and the air Since the air supply device AFD for ejecting air from the air ejection hole 12a2 is connected to the ejection hole 12a2, even when the electronic component EC taken into the one-dimensional passage C1 is clogged by the throttle NP. The electronic component EC clogged in the throttle portion NP by the air jetted from the air ejection hole 12a2 into the one-dimensional passage C1 can be blown upward from the throttle portion NP to eliminate the clogging.
さらに、前述のバルクフィーダによれば、前記エア供給装置AFDはエア噴出に係るエアの供給及び停止を制御する噴出バルブGVを所定の開時間to及び閉時間tcに基づいて間欠的に開閉し得るようにその動作を制御するコントローラCONを有しているので、該噴出バルブGVの開時間to及び閉時間tcを適宜設定することによって、バルクフィーダによる所期の整列供給動作に支障を生じることなく、該整列供給動作の途中で絞り部NPに詰まった電子部品ECを該絞り部NPから上方に吹き上げて詰まりを解消する動作を自動的に行うことができる。 Furthermore, according to the above-described bulk feeder, the air supply device AFD can intermittently open and close the ejection valve GV for controlling the supply and stop of the air related to the air ejection based on the predetermined opening time to and closing time tc. Thus, the controller CON for controlling the operation of the ejection valve GV can be set as appropriate so that the opening time to and the closing time tc of the ejection valve GV are appropriately set without causing any trouble in the intended alignment supply operation by the bulk feeder. In the course of the alignment supply operation, the electronic component EC clogged in the narrowed portion NP can be automatically blown upward from the narrowed portion NP to automatically eliminate the clogging.
さらに、前述のバルクフィーダによれば、前記絞り部NPが1次元通路C1の隣接する2面に設けられた突起11g,12a1によって構成されているので、絞り部NPを構成するために複雑な加工及び成形を必要としない。
Furthermore, according to the above-described bulk feeder, since the narrowed portion NP is constituted by the
尚、前述の説明では、エア噴出孔12a2を1次元通路C1と直交する向きで設けたものを示したが、図7(A)に示すようにエア噴出孔12a2’を絞り部NPに向かう向きで斜めに設けてもよい。このようにすれば、エア噴出孔12a2’から噴出されるエアを直接的に絞り部NPに詰まった電子部品ECに吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。 In the above description, the air ejection hole 12a2 is provided in a direction orthogonal to the one-dimensional passage C1, but as shown in FIG. 7A, the air ejection hole 12a2 ′ is directed toward the throttle portion NP. May be provided at an angle. In this way, the air ejected from the air ejection holes 12a2 'can be blown directly onto the electronic component EC clogged in the throttle portion NP, and the electronic component EC can be effectively blown up.
また、前述の説明では、絞り部NPを縦断面台形の突起12a1によって構成したものを示したが、図7(B)に示すように縦断面三角形の突起12a1’によって絞り部NP’を構成してもよい。このようにすれば、絞り部NP’と該絞り部NP’に詰まった電子部品ECとの接触抵抗を減らして、エアによる該電子部品ECの吹き上げをスムースに行うことができる。 In the above description, the diaphragm portion NP is constituted by the trapezoidal protrusion 12a1 having a vertical cross section. However, as shown in FIG. 7B, the throttle portion NP ′ is constituted by a protrusion 12a1 ′ having a triangular cross section. May be. By doing so, it is possible to reduce the contact resistance between the narrowed portion NP ′ and the electronic component EC clogged in the narrowed portion NP ′, and to smoothly blow up the electronic component EC by air.
さらに、前述の説明では、エア噴出孔12a2を1次元通路C1と直交する向きで設けて所定の噴出タイミングで該エア噴出孔12a2から1次元通路C1内にエアを噴出するようにしたが、図7(C)に示すように1次元通路C1のエア噴出孔12a2の下側(下流側)を閉塞可能なシャッター板15を第1カバープレート12aに形成したスリット12a3に横移動可能に設け、該シャッター板15をソレノイド等の駆動源によって横移動できるように構成し、エア噴出孔12a2から1次元通路C1内にエアが噴出されるタイミングでシャッター板15によって1次元通路C1のエア噴出孔12a2の下側(下流側)を閉塞するようにすれば、エア噴出孔12a2から1次元通路C1内に噴出されるエアを絞り部NPに詰まった電子部品ECに集中して吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。
Furthermore, in the above description, the air ejection holes 12a2 are provided in a direction orthogonal to the one-dimensional passage C1, and air is ejected from the air ejection holes 12a2 into the one-dimensional passage C1 at a predetermined ejection timing. 7 (C), a
さらに、前述の説明では、エア噴出孔12a2から1次元通路C1内へのエアの噴出を間欠的に行うものを示したが、(1)絞り部NPに電子部品ECが詰まったときのみにエア供給装置の噴出バルブを手動操作で開として所期のエア噴出を行うことによって詰まりを解消するようにしたり、(2)絞り部NPの下側(下流側)に該絞り部NPに電子部品ECが詰まったことを検知するための光センサを設けて、該光センサによって詰まりが検出されたときのみにコントローラによってエア供給装置の噴出バルブを一定時間開として所期のエア噴出を行うことによって詰まりを解消するようにしてもよい。 Further, in the above description, the air is intermittently ejected from the air ejection hole 12a2 into the one-dimensional passage C1, but (1) the air only when the electronic part EC is clogged in the throttle NP. The clogging can be eliminated by manually opening the ejection valve of the supply device and performing the desired air ejection, or (2) the electronic part EC is placed on the throttle part NP below (on the downstream side) the throttle part NP. An optical sensor is provided for detecting that the air supply is clogged, and only when the clogging is detected by the optical sensor, the controller opens the injection valve of the air supply device for a certain period of time and performs the desired air injection. May be eliminated.
さらに、前述の説明では、長さL(基準長さ±公差)>幅W(基準幅±公差)=高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECに適合したものを示したが、2次元室C2の間隔を高さHの最大寸法よりも僅かに大きく、且つ、幅Wの最大寸法よりも小さな間隔とすると共に1次元通路C1の横断面形を変更すれば、長さL(基準長さ±公差)>幅W(基準幅±公差)>高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECを前記同様の動作で整列し供給することができ、且つ、前記同様の詰まり解消効果も得ることができる。 Further, in the above description, the electronic component EC having a cuboid shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance) = height H (reference height ± tolerance) is used. Although shown in conformity, the interval of the two-dimensional chamber C2 is slightly larger than the maximum dimension of the height H and smaller than the maximum dimension of the width W, and the cross-sectional shape of the one-dimensional passage C1 is If changed, an electronic component EC having a rectangular parallelepiped shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance)> height H (reference height ± tolerance) is the same as described above. It is possible to align and supply by operation, and to obtain the same clogging elimination effect as described above.
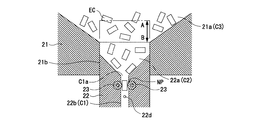
[第2実施形態]
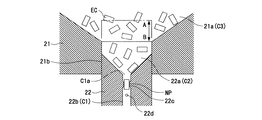
図8は本発明(バルクフィーダ)の第2実施形態を示す、バルクフィーダの縦断面図である。図8中の符号21はホッパー、22はスライダ、ECは電子部品である。電子部品ECは第1実施形態で説明したものと同じであるのでここでの説明を省略する。
[Second Embodiment]
FIG. 8 is a longitudinal sectional view of a bulk feeder showing a second embodiment of the present invention (bulk feeder). In FIG. 8,
まず、図8を参照してバルクフィーダのメカニズムについて説明する。ここでの説明では図8の手前を前、奥を後、左を左、右を右と表記する。 First, the mechanism of the bulk feeder will be described with reference to FIG. In the description here, the front of FIG. 8 is represented as the front, the back is the rear, the left is the left, and the right is the right.
ホッパー21は、上部に3次元室C3を構成する縦断面ベース形の凹部21aを有し、該凹部21aの下側にスライダ22を上下移動可能に受容する矩形孔21bを有している。3次元室C3は電子部品ECをその姿勢を制限すること無しに収納できる形状を成していて、3次元室C3内に収納された電子部品ECは該3次元室C3内をランダムな姿勢で自由に移動することができる。
The
スライダ22は外形が矩形で、上部に2次元室C2を構成する縦断面ベース形の凹部22aを有し、該凹部22aの下側に1次元通路C1を構成する横断面矩形の通路22bを有している。2次元室C2は電子部品ECの幅Wの最大寸法と高さHの最大寸法よりも僅かに大きな間隔を有する平行スペースから成り、3次元室C3から2次元室C2内に取り込まれた電子部品ECは該2次元室C2内を幅W及び高さHの向きが揃った姿勢で移動することができる。1次元通路C1は電子部品ECの幅Wの最大寸法よりも僅かに大きな面と高さHの最大寸法よりも僅かに大きな面が隣り合う横断面矩形の通路から成り、2次元室C2から1次元通路C1内に取り込まれた電子部品ECは該1次元通路C1内を幅W,高さH及び長さの向きが揃った姿勢で自重により下方移動することができる。
The
前記1次元通路C1は前記2次元室C2との境界をその入口C1aとしており、該入口C1aの下側(下流側)には該1次元通路C1の横断面形を局部的に小さくした横断面形を有する絞り部NPが形成されている。この絞り部NPは、前記1次元通路C1の4つの内面に設けられた縦断面台形の突起22cによって構成されている。また、絞り部NPの横断面形は1次元通路C1の横断面形と相似の矩形であり、該絞り部NPの隣接する2つの内面の寸法は電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きく設定されている。
The one-dimensional passage C1 has a boundary with the two-dimensional chamber C2 as an inlet C1a, and a cross section in which the cross-sectional shape of the one-dimensional passage C1 is locally reduced on the lower side (downstream side) of the inlet C1a. An aperture NP having a shape is formed. The narrowed portion NP is constituted by a
また、前記1次元通路C1の絞り部NPの下側(下流側)には、1次元通路C1内にエアを噴出するためのエア噴出孔22dが前記1次元通路C1の1つの内面に該1次元通路C1と直交する向きで設けられている。図示を省略したが、このエア噴出孔22dには、該エア噴出孔22dからのエアの噴出を行うための第1実施形態と同様のエア供給装置AFDがエア配管を介して接続されている。
Further, an
次に、図8を参照してバルクフィーダによる電子部品ECの整列供給動作について説明する。 Next, the operation of aligning and supplying the electronic components EC by the bulk feeder will be described with reference to FIG.
バルクフィーダによる電子部品ECの整列供給動作は、良品寸法の電子部品EC、即ち、長さLと幅Wと高さHのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる電子部品ECを3次元室C3内に収納した後に、スライダ22を図8中でA方向に所定距離変位させ、且つ、変位後にB方向に同一距離変位させて復帰させる動作を連続的或いは間欠的に行うと共に、エア噴出孔22dから1次元通路C1内に間欠的にエアを噴出する動作を行うことによって実行される。
The operation of aligning and supplying the electronic components EC by the bulk feeder is a non-defective electronic component EC, that is, the length L, the width W, and the height H are the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance. After the electronic component EC that fits in is stored in the three-dimensional chamber C3, the
スライダ22の前記動作によって、3次元室C3内に収納されている電子部品ECは該3次元室C3から2次元室C2内に幅W及び高さHの向きが揃った姿勢で取り込まれる。前記動作においてスライダ22の上部は3次元室C3内に突出するため、3次元室C3内に収納されている電子部品ECはスライダ22の上部突出による撹拌によってその幅W及び高さHの向きを変化して2次元室C2内に取り込まれるような作用を生じる。また、スライダ22の前記動作によって、2次元室C2内に取り込まれた電子部品ECは該2次元室C2から1次元通路C1内に幅W,高さH及び長さの向きが揃った姿勢で取り込まれる。前記動作においてスライダ22は上下移動をするため、この上下移動による振動等によって2次元室C2内に取り込まれた電子部品ECはその長さLの向きを変化して1次元通路C1内に取り込まれるような作用を生じる。
By the operation of the
1次元通路C1内に取り込まれた電子部品ECは幅W,高さH及び長さLの向きが揃った姿勢で該1次元通路C1内を自重により下方移動する。1次元通路C1の入口C1aの下側(下流側)には絞り部NPが存在するが、1次元通路C1内に取り込まれた電子部品ECの幅W,高さH及び長さLのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる場合、該電子部品ECは絞り部NPを通過する。 The electronic component EC taken into the one-dimensional passage C1 moves downward in the one-dimensional passage C1 by its own weight in a posture in which the directions of the width W, the height H, and the length L are aligned. The throttle NP is present below (downstream) the inlet C1a of the one-dimensional passage C1, but the width W, height H, and length L of the electronic component EC taken into the one-dimensional passage C1 are respectively determined. When the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance are satisfied, the electronic component EC passes through the aperture NP.
バルクフィーダの3次元室C3内には必要に応じて電子部品ECが補充されることから、補充の際に外部から3次元室C3内に入り込んだ塵埃や、補充の際或いはその前後で電子部品ECから剥がれ落ちた欠片等が、3次元室C3内に収納されている電子部品ECに付着する恐れがある。依って、前述の整列供給動作によって1次元通路C1内に取り込まれた電子部品ECに前記の塵埃や欠片等が付着していて幅Wと高さHの少なくとも一方の外観上寸法が絞り部NPを通過できない程度まで増していると、該電子部品ECは1次元通路C1を移動する過程で絞り部NPで詰まって停止する。 Since the electronic component EC is replenished in the three-dimensional chamber C3 of the bulk feeder as necessary, the dust that has entered the three-dimensional chamber C3 from the outside during the replenishment, and the electronic component at the time of replenishment, or before and after that. There is a possibility that a piece or the like peeled off from the EC adheres to the electronic component EC stored in the three-dimensional chamber C3. Therefore, the dust, chips, and the like are attached to the electronic component EC taken into the one-dimensional passage C1 by the above-described alignment supply operation, and at least one of the external dimensions of the width W and the height H is the narrowed portion NP. If it has increased to such an extent that it cannot pass through the electronic component EC, the electronic component EC is clogged by the throttle portion NP and stopped in the process of moving through the one-dimensional passage C1.
前述の整列供給動作に併せてエア噴出孔22dから1次元通路C1内に間欠的に噴出されるエアは、1次元通路C1内に取り込まれた電子部品ECが絞り部NPで詰まって停止したときに、該電子部品ECを絞り部NPから上方に吹き上げて詰まりを解消する作用を発揮する。エアを間欠的に噴出する理由は非噴出時間を利用して前記の整列供給動作を支障なく行うことにあり、以下この点については第1実施形態で述べた通りであるのでここでの説明を省略する。 The air intermittently ejected into the one-dimensional passage C1 from the air ejection holes 22d in conjunction with the above-described alignment supply operation is stopped when the electronic component EC taken into the one-dimensional passage C1 is clogged with the throttle NP. In addition, the electronic component EC is blown upward from the narrowed portion NP to exert an action of eliminating clogging. The reason why the air is intermittently ejected is to perform the alignment supply operation without any trouble by using the non-ejection time. Since this point is the same as described in the first embodiment, the explanation here will be given. Omitted.
このように、前述のバルクフィーダによれば、前記1次元通路C1の入口C1aの下側(下流側)に該1次元通路C1の横断面形を局部的に小さくした横断面形を有し、且つ、幅Wが基準幅+公差で高さHが基準高さ+公差の電子部品の通過を許容する絞り部NPを設けてあるので、1次元通路C1内に取り込まれた電子部品ECに塵埃や欠片等が付着していて幅Wと高さHの少なくとも一方の外観上寸法が絞り部NPを通過できない程度まで増している場合に該電子部品ECを1次元通路C1の絞り部NPの位置で積極的に詰まらせることができる。 Thus, according to the above-mentioned bulk feeder, it has a cross-sectional shape in which the cross-sectional shape of the one-dimensional passage C1 is locally reduced on the lower side (downstream side) of the inlet C1a of the one-dimensional passage C1. In addition, since the narrowed portion NP that allows passage of the electronic component having the width W of the reference width + tolerance and the height H of the reference height + tolerance is provided, the electronic component EC taken into the one-dimensional passage C1 has dust. If the electronic component EC is increased to such an extent that at least one of the width W and the height H cannot be passed through the throttle NP, the electronic component EC is positioned at the throttle NP of the one-dimensional passage C1. Can be actively clogged with.
換言すれば、部品詰まりの原因となる電子部品ECが1次元通路C1内に取り込まれた場合でも該電子部品ECを常に同じ位置(絞り部NPの位置)で詰まらせることができるので、部品詰まりが生じている位置を探索する必要がないし、また、部品詰まりを生じる位置が定まっているいるので部品詰まりを解消する作業を迅速に行うことができる。従って、部品詰まりに伴う位置探索及び詰まり解消の作業を簡便化して、詰まり解消を極めて簡単に行うことができる。 In other words, even when the electronic component EC causing the component clogging is taken into the one-dimensional passage C1, the electronic component EC can always be clogged at the same position (the position of the narrowed portion NP). It is not necessary to search for the position where the clogging occurs, and the position where the clogging occurs is fixed, so that the work for eliminating the clogging can be quickly performed. Therefore, it is possible to simplify the position search and clogging work that accompanies clogging of the parts, and to clog clogging very easily.
また、前述のバルクフィーダによれば、前記1次元通路C1の絞り部NPの下側(下流側)に該1次元通路C1内にエアを噴出するためのエア噴出孔22dを設けると共に、このエア噴出孔22dに該エア噴出孔22dからのエアの噴出を行うためのエア供給装置AFDを接続してあるので、1次元通路C1内に取り込まれた電子部品ECが絞り部NPで詰まった場合でも、エア噴出孔22dから1次元通路C1内に噴出されるエアによって絞り部NPで詰まった電子部品ECを該絞り部NPから上方に吹き上げて詰まりを解消することができる。
Further, according to the above-described bulk feeder, the
さらに、前述のバルクフィーダによれば、前記エア供給装置AFDはエア噴出に係るエアの供給及び停止を制御する噴出バルブGVを所定の開時間to及び閉時間tcに基づいて間欠的に開閉し得るようにその動作を制御するコントローラCONを有しているので、該噴出バルブGVの開時間to及び閉時間tcを適宜設定することによって、バルクフィーダによる所期の整列供給動作に支障を生じることなく、該整列供給動作の途中で絞り部NPに詰まった電子部品ECを該絞り部NPから上方に吹き上げて詰まりを解消する動作を自動的に行うことができる。 Furthermore, according to the above-described bulk feeder, the air supply device AFD can intermittently open and close the ejection valve GV for controlling the supply and stop of the air related to the air ejection based on the predetermined opening time to and closing time tc. Thus, the controller CON for controlling the operation of the ejection valve GV can be set as appropriate so that the opening time to and the closing time tc of the ejection valve GV are appropriately set without causing any trouble in the intended alignment supply operation by the bulk feeder. In the course of the alignment supply operation, the electronic component EC clogged in the narrowed portion NP can be automatically blown upward from the narrowed portion NP to automatically eliminate the clogging.
尚、前述の説明では、エア噴出孔22dを1次元通路C1と直交する向きで設けたものを示したが、図7(A)に示したものと同様に、エア噴出孔を絞り部NPに向かう向きで斜めに設けてもよい。このようにすれば、エア噴出孔から噴出されるエアを直接的に絞り部NPに詰まった電子部品ECに吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。
In the above description, the
また、前述の説明では、絞り部NPを縦断面台形の突起22cによって構成したものを示したが、図7(B)に示したものと同様に、縦断面三角形の突起によって絞り部NPを構成してもよい。このようにすれば、絞り部NPと該絞り部NPに詰まった電子部品ECとの接触抵抗を減らして、エアによる該電子部品ECの吹き上げをスムースに行うことができる。
Further, in the above description, the diaphragm portion NP is configured by the
さらに、前述の説明では、エア噴出孔22dを1次元通路C1と直交する向きで設けて所定の噴出タイミングで該エア噴出孔22dから1次元通路C1内にエアを噴出するようにしたが、図7(C)に示したものと同様に、1次元通路C1のエア噴出孔22dの下側(下流側)を閉塞可能なシャッター板をスライダ22に形成したスリットに横移動可能に設け、該シャッター板をソレノイド等の駆動源によって横移動できるように構成し、エア噴出孔22dから1次元通路C1内にエアが噴出されるタイミングでシャッター板によって1次元通路C1のエア噴出孔22dの下側(下流側)を閉塞するようにすれば、エア噴出孔22dから1次元通路C1内に噴出されるエアを絞り部NPに詰まった電子部品ECに集中して吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。
Further, in the above description, the air ejection holes 22d are provided in a direction orthogonal to the one-dimensional passage C1, and air is ejected from the air ejection holes 22d into the one-dimensional passage C1 at a predetermined ejection timing. 7 (C), a shutter plate capable of closing the lower side (downstream side) of the
さらに、前述の説明では、エア噴出孔22dから1次元通路C1内へのエアの噴出を間欠的に行うものを示したが、(1)絞り部NPに電子部品ECが詰まったときのみにエア供給装置の噴出バルブを手動操作で開として所期のエア噴出を行うことによって詰まりを解消するようしたり、(2)絞り部NPの下側(下流側)に該絞り部NPに電子部品ECが詰まったことを検知するための光センサを設けて、該光センサによって詰まりが検出されたときのみにコントローラによってエア供給装置の噴出バルブを所定時間だけ開として所期のエア噴出を行うことによって詰まりを解消するようにしてもよい。
Further, in the above description, the air is intermittently ejected from the
さらに、前述の説明では、長さL(基準長さ±公差)>幅W(基準幅±公差)=高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECに適合したものを示したが、2次元室C2の間隔を高さHの最大寸法よりも僅かに大きく、且つ、幅Wの最大寸法よりも小さな間隔とすると共に1次元通路C1の横断面形を変更すれば、長さL(基準長さ±公差)>幅W(基準幅±公差)>高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECを前記同様の動作で整列し供給することができ、且つ、前記同様の詰まり解消効果も得ることができる。 Further, in the above description, the electronic component EC having a cuboid shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance) = height H (reference height ± tolerance) is used. Although shown in conformity, the interval of the two-dimensional chamber C2 is slightly larger than the maximum dimension of the height H and smaller than the maximum dimension of the width W, and the cross-sectional shape of the one-dimensional passage C1 is If changed, an electronic component EC having a rectangular parallelepiped shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance)> height H (reference height ± tolerance) is the same as described above. It is possible to align and supply by operation, and to obtain the same clogging elimination effect as described above.
[第3実施形態]
図9は本発明(バルクフィーダ)の第3実施形態を示す、バルクフィーダの縦断面図である。
[Third Embodiment]
FIG. 9 is a longitudinal sectional view of a bulk feeder showing a third embodiment of the present invention (bulk feeder).
第3実施形態が第2実施形態と異なるところは、1次元通路C1の相対する2つの内面或いは4つの内面それぞれにその一部が1次元通路C1内に突出するようにローラ23を回転自在に配置して、2つ或いは4つのローラ23によって絞り部NPを構成した点にある。ローラ23が2つの場合、相対する2つのローラ23の対向間隔は電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きく設定されている。また、ローラ23が4つの場合、相対する2つのローラ23の対向間隔と他の2つのローラ23の対向間隔は電子部品ECの幅Wの最大寸法(=基準幅+公差)と高さHの最大寸法(=基準高さ+公差)よりも僅かに大きく設定されている。他の構成は第2実施形態と同じであるので同一符号を用いてその説明を省略する。
The third embodiment is different from the second embodiment in that the
バルクフィーダによる電子部品ECの整列供給動作は、良品寸法の電子部品EC、即ち、長さLと幅Wと高さHのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる電子部品ECを3次元室C3内に収納した後に、スライダ22を図9中でA方向に所定距離変位させ、且つ、変位後にB方向に同一距離変位させて復帰させる動作を連続的或いは間欠的に行うと共に、エア噴出孔22dから1次元通路C1内に間欠的にエアを噴出する動作を行うことによって実行される。
The operation of aligning and supplying the electronic components EC by the bulk feeder is a non-defective electronic component EC, that is, the length L, the width W, and the height H are the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance. After the electronic component EC that fits in the three-dimensional chamber C3 is stored in the three-dimensional chamber C3, the
スライダ22の前記動作によって、3次元室C3内に収納されている電子部品ECは該3次元室C3から2次元室C2内に幅W及び高さHの向きが揃った姿勢で取り込まれる。前記動作においてスライダ22の上部は3次元室C3内に突出するため、3次元室C3内に収納されている電子部品ECはスライダ22の上部突出による撹拌によってその幅W及び高さHの向きを変化して2次元室C2内に取り込まれるような作用を生じる。また、スライダ22の前記動作によって、2次元室C2内に取り込まれた電子部品ECは該2次元室C2から1次元通路C1内に幅W,高さH及び長さの向きが揃った姿勢で取り込まれる。前記動作においてスライダ22は上下移動をするため、この上下移動による振動等によって2次元室C2内に取り込まれた電子部品ECはその長さLの向きを変化して1次元通路C1内に取り込まれるような作用を生じる。
By the operation of the
1次元通路C1内に取り込まれた電子部品ECは幅W,高さH及び長さLの向きが揃った姿勢で該1次元通路C1内を自重により下方移動する。1次元通路C1の入口C1aの下側(下流側)には絞り部NPが存在するが、1次元通路C1内に取り込まれた電子部品ECの幅W,高さH及び長さLのそれぞれが基準長さ±公差と基準幅±公差と基準高さ±公差に収まる場合、該電子部品ECは絞り部NPを通過する。 The electronic component EC taken into the one-dimensional passage C1 moves downward in the one-dimensional passage C1 by its own weight in a posture in which the directions of the width W, the height H, and the length L are aligned. The throttle NP is present below (downstream) the inlet C1a of the one-dimensional passage C1, but the width W, height H, and length L of the electronic component EC taken into the one-dimensional passage C1 are respectively determined. When the reference length ± tolerance, reference width ± tolerance, and reference height ± tolerance are satisfied, the electronic component EC passes through the aperture NP.
バルクフィーダの3次元室C3内には必要に応じて電子部品ECが補充されることから、補充の際に外部から3次元室C3内に入り込んだ塵埃や、補充の際或いはその前後で電子部品ECから剥がれ落ちた欠片等が、3次元室C3内に収納されている電子部品ECに付着する恐れがある。依って、前述の整列供給動作によって1次元通路C1内に取り込まれた電子部品ECに前記の塵埃や欠片等が付着していて幅Wと高さHの少なくとも一方の外観上寸法が絞り部NPを通過できない程度まで増していると、該電子部品ECは1次元通路C1を移動する過程で絞り部NPにて詰まって停止する。 Since the electronic component EC is replenished in the three-dimensional chamber C3 of the bulk feeder as necessary, the dust that has entered the three-dimensional chamber C3 from the outside during the replenishment, and the electronic component at the time of replenishment, or before and after that. There is a possibility that a piece or the like peeled off from the EC adheres to the electronic component EC stored in the three-dimensional chamber C3. Therefore, the dust, chips, and the like are attached to the electronic component EC taken into the one-dimensional passage C1 by the above-described alignment supply operation, and at least one of the external dimensions of the width W and the height H is the narrowed portion NP. If it has increased to such an extent that it cannot pass through the electronic component EC, the electronic component EC is clogged and stopped at the throttle portion NP in the process of moving through the one-dimensional passage C1.
前述の整列供給動作に併せてエア噴出孔22dから1次元通路C1内に間欠的に噴出されるエアは、1次元通路C1内に取り込まれた電子部品ECが絞り部NPで詰まって停止したときに、該電子部品ECを絞り部NPから上方に吹き上げて詰まりを解消する作用を発揮する。エアを間欠的に噴出する理由は非噴出時間を利用して前記の整列供給動作を支障なく行うことにあり、以下この点については第1実施形態で述べた通りであるのでここでの説明を省略する。 The air intermittently ejected into the one-dimensional passage C1 from the air ejection holes 22d in conjunction with the above-described alignment supply operation is stopped when the electronic component EC taken into the one-dimensional passage C1 is clogged with the throttle NP. In addition, the electronic component EC is blown upward from the narrowed portion NP to exert an action of eliminating clogging. The reason why the air is intermittently ejected is to perform the alignment supply operation without any trouble by using the non-ejection time. Since this point is the same as described in the first embodiment, the explanation here will be given. Omitted.
このように、前述のバルクフィーダによれば、絞り部NPの構成が異なるものの、第2実施形態と同様の作用効果を発揮することができる。 As described above, according to the above-described bulk feeder, although the configuration of the narrowed portion NP is different, the same operational effects as those of the second embodiment can be exhibited.
また、前述のバルクフィーダによれば、前記絞り部NPが回転自在な複数のローラ23によって構成されているので、ローラ23の回転を利用して絞り部NPに詰まった電子部品ECの吹き上げをスムースに行うことができる。
Further, according to the above-described bulk feeder, since the aperture portion NP is constituted by a plurality of freely
尚、前述の説明では、エア噴出孔22dを1次元通路C1と直交する向きで設けたものを示したが、図7(A)に示したものと同様に、エア噴出孔を絞り部NPに向かう向きで斜めに設けてもよい。このようにすれば、エア噴出孔から噴出されるエアを直接的に絞り部NPに詰まった電子部品ECに吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。
In the above description, the
また、前述の説明では、エア噴出孔22dを1次元通路C1と直交する向きで設けて所定の噴出タイミングで該エア噴出孔22dから1次元通路C1内にエアを噴出するようにしたが、図7(C)に示したものと同様に、1次元通路C1のエア噴出孔22dの下側(下流側)を閉塞可能なシャッター板をスライダ22に形成したスリットに横移動可能に設け、該シャッター板をソレノイド等の駆動源によって横移動できるように構成し、エア噴出孔22dから1次元通路C1内にエアが噴出されるタイミングでシャッター板によって1次元通路C1のエア噴出孔22dの下側(下流側)を閉塞するようにすれば、エア噴出孔22dから1次元通路C1内に噴出されるエアを絞り部NPに詰まった電子部品ECに集中して吹き付けて、該電子部品ECの吹き上げを効果的に行うことができる。
In the above description, the air ejection holes 22d are provided in a direction orthogonal to the one-dimensional passage C1, and air is ejected from the air ejection holes 22d into the one-dimensional passage C1 at a predetermined ejection timing. 7 (C), a shutter plate capable of closing the lower side (downstream side) of the
さらに、前述の説明では、エア噴出孔22dから1次元通路C1内へのエアの噴出を間欠的に行うものを示したが、(1)絞り部NPに電子部品ECが詰まったときのみにエア供給装置の噴出バルブを手動操作で開として所期のエア噴出を行うことによって詰まりを解消するようしたり、(2)絞り部NPの下側(下流側)に該絞り部NPに電子部品ECが詰まったことを検知するための光センサを設けて、該光センサによって詰まりが検出されたときのみにコントローラによってエア供給装置の噴出バルブを一定時間開として所期のエア噴出を行うことによって詰まりを解消するようにしてもよい。
Further, in the above description, the air is intermittently ejected from the
さらに、前述の説明では、長さL(基準長さ±公差)>幅W(基準幅±公差)=高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECに適合したものを示したが、2次元室C2の間隔を高さHの最大寸法よりも僅かに大きく、且つ、幅Wの最大寸法よりも小さな間隔とすると共に1次元通路C1の横断面形を変更すれば、長さL(基準長さ±公差)>幅W(基準幅±公差)>高さH(基準高さ±公差)の寸法関係を有する直方体形状を成す電子部品ECを前記同様の動作で整列し供給することができ、且つ、前記同様の詰まり解消効果も得ることができる。 Further, in the above description, the electronic component EC having a cuboid shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance) = height H (reference height ± tolerance) is used. Although shown in conformity, the interval of the two-dimensional chamber C2 is slightly larger than the maximum dimension of the height H and smaller than the maximum dimension of the width W, and the cross-sectional shape of the one-dimensional passage C1 is If changed, an electronic component EC having a rectangular parallelepiped shape having a dimensional relationship of length L (reference length ± tolerance)> width W (reference width ± tolerance)> height H (reference height ± tolerance) is the same as described above. It is possible to align and supply by operation, and to obtain the same clogging elimination effect as described above.
EC…電子部品、C3…3次元室、C2…2次元室、C1…1次元通路、NP,NP’…絞り部、11g,12a1,12a1’,22c…突起、12a2,12a2’…エア噴出孔、23…ローラ、AFD…エア供給装置、GV…噴出バルブ、CON…コントローラ。 EC: electronic component, C3: three-dimensional chamber, C2: two-dimensional chamber, C1: one-dimensional passage, NP, NP '... throttle part, 11g, 12a1, 12a1', 22c ... projection, 12a2, 12a2 '... air ejection hole , 23 ... roller, AFD ... air supply device, GV ... jetting valve, CON ... controller.
Claims (11)
前記1次元通路の所定位置に設けられ、該1次元通路の横断面形を局部的に小さくした横断面形を有し、且つ、幅が基準幅+公差で高さが基準高さ+公差の電子部品の通過を許容する絞り部を備えている、
ことを特徴とするバルクフィーダ。 Dimensional relationship of length> width = height or length>width> height dimensional relationship, a three-dimensional chamber for storing the electronic components in a rectangular shape, and a width of the electronic components in the three-dimensional chamber And a two-dimensional chamber for taking in a posture in which the directions of height are aligned, and a transverse cross-sectional rectangle for taking in and moving the electronic components in the two-dimensional chamber in a posture in which the directions of width, height, and length are aligned A bulk feeder with a one-dimensional passage of
The cross-sectional shape is provided at a predetermined position of the one-dimensional passage, the cross-sectional shape of the one-dimensional passage is locally reduced, and the width is a reference width + tolerance and the height is a reference height + tolerance. It has a diaphragm that allows electronic parts to pass through.
A bulk feeder characterized by that.
前記エア噴出孔に接続され、該エア噴出孔からのエアの噴出を行うためのエア供給装置とをさらに備えている、
ことを特徴とする請求項1に記載のバルクフィーダ。 An air ejection hole provided on the downstream side of the throttle portion of the one-dimensional passage, for ejecting air into the one-dimensional passage;
An air supply device connected to the air ejection hole for ejecting air from the air ejection hole;
The bulk feeder according to claim 1.
ことを特徴とする請求項2に記載のバルクフィーダ。 The air supply device has an ejection valve that controls supply and stop of air related to the air ejection,
The bulk feeder according to claim 2.
ことを特徴とする請求項3に記載のバルクフィーダ。 The air supply device has a controller that controls the operation so that the ejection valve can be opened and closed intermittently based on a predetermined opening time and closing time.
The bulk feeder according to claim 3.
前記エア供給装置は、光センサによって詰まりが検出されたときのみにエア供給装置の噴出バルブを所定時間だけ開とするコントローラを有している、
ことを特徴とする請求項3に記載のバルクフィーダ。 An optical sensor provided on the downstream side of the throttle portion of the one-dimensional passage, for detecting that the throttle portion is clogged with electronic components;
The air supply device has a controller that opens the ejection valve of the air supply device for a predetermined time only when clogging is detected by the optical sensor.
The bulk feeder according to claim 3.
ことを特徴とする請求項1〜5の何れか1項に記載のバルクフィーダ。 The throttle portion is constituted by a protrusion provided on at least two adjacent inner surfaces of the one-dimensional passage.
The bulk feeder of any one of Claims 1-5 characterized by the above-mentioned.
ことを特徴とする請求項6に記載のバルクフィーダ。 The protrusion has a trapezoidal longitudinal section,
The bulk feeder according to claim 6.
ことを特徴とする請求項6に記載のバルクフィーダ。 The protrusion has a longitudinal cross-sectional triangle,
The bulk feeder according to claim 6.
ことを特徴とする請求項1〜5の何れか1項に記載のバルクフィーダ。 The throttle portion is configured by a roller that is rotatably provided on at least two opposing inner surfaces of the one-dimensional passage so that a part thereof protrudes into the one-dimensional passage.
The bulk feeder of any one of Claims 1-5 characterized by the above-mentioned.
ことを特徴とする請求項1〜9の何れか1項に記載のバルクフィーダ。 The air ejection hole is provided on one inner surface of the one-dimensional passage in a direction orthogonal to the one-dimensional passage.
The bulk feeder according to claim 1, wherein:
ことを特徴とする請求項1〜9の何れか1項に記載のバルクフィーダ。 The air ejection hole is provided on one inner surface of the one-dimensional passage in a direction toward the throttle portion.
The bulk feeder according to claim 1, wherein:
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008001239A JP2009164381A (en) | 2008-01-08 | 2008-01-08 | Bulk feeder |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008001239A JP2009164381A (en) | 2008-01-08 | 2008-01-08 | Bulk feeder |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| JP2009164381A true JP2009164381A (en) | 2009-07-23 |
Family
ID=40966649
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2008001239A Withdrawn JP2009164381A (en) | 2008-01-08 | 2008-01-08 | Bulk feeder |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP2009164381A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2022147614A (en) * | 2021-03-23 | 2022-10-06 | 株式会社村田製作所 | Parts storage device |
-
2008
- 2008-01-08 JP JP2008001239A patent/JP2009164381A/en not_active Withdrawn
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2022147614A (en) * | 2021-03-23 | 2022-10-06 | 株式会社村田製作所 | Parts storage device |
| JP7400762B2 (en) | 2021-03-23 | 2023-12-19 | 株式会社村田製作所 | Parts storage device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6879598B2 (en) | Paper leaf transport device | |
| JP2008228947A (en) | Plate structure of game board for pinball game machine | |
| JP6211159B2 (en) | Paper sheet transport device | |
| TWI523803B (en) | Parts feeder | |
| JP6267777B1 (en) | Blanking lower mold | |
| JP6051489B2 (en) | Auxiliary blower for paper sheet transport device, | |
| JP2005349543A (en) | Screw supplying device | |
| JP5431529B2 (en) | Bullet ball machine | |
| JP6963809B2 (en) | Guide rail for bolts | |
| JP5296038B2 (en) | Lattice core material manufacturing apparatus, manufacturing method, and flash panel | |
| JP2008206814A (en) | Game machine | |
| JP2015062610A (en) | Game machine | |
| JP7240143B2 (en) | Cutting device | |
| JP7044618B2 (en) | Etching device | |
| JP2017154188A (en) | Machining device | |
| WO2025169610A1 (en) | Storage case | |
| JP2012245384A (en) | Token pusher game device | |
| JP2011152481A (en) | Game machine | |
| JPWO2019244294A1 (en) | Tape feeder | |
| JP2009183584A (en) | Frame body for game machine | |
| JP2003331336A (en) | Coin ejection device | |
| JP2008079761A (en) | Frame structure of pinball game machine | |
| RS59085B1 (en) | Guiding device | |
| JP2010113684A (en) | Product dispensing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A300 | Withdrawal of application because of no request for examination |
Free format text: JAPANESE INTERMEDIATE CODE: A300 Effective date: 20110405 |