EP4389707B1 - Method for recycling ferrous sulfate heptahydrate and sulfuric acid from waste acid in titanium dioxide production - Google Patents
Method for recycling ferrous sulfate heptahydrate and sulfuric acid from waste acid in titanium dioxide production Download PDFInfo
- Publication number
- EP4389707B1 EP4389707B1 EP23216801.3A EP23216801A EP4389707B1 EP 4389707 B1 EP4389707 B1 EP 4389707B1 EP 23216801 A EP23216801 A EP 23216801A EP 4389707 B1 EP4389707 B1 EP 4389707B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- acid
- ferrous sulfate
- titanium dioxide
- waste
- dioxide production
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C01—INORGANIC CHEMISTRY
- C01G—COMPOUNDS CONTAINING METALS NOT COVERED BY SUBCLASSES C01D OR C01F
- C01G1/00—Methods of preparing compounds of metals not covered by subclasses C01B, C01C, C01D, or C01F, in general
- C01G1/10—Sulfates
-
- C—CHEMISTRY; METALLURGY
- C01—INORGANIC CHEMISTRY
- C01B—NON-METALLIC ELEMENTS; COMPOUNDS THEREOF; METALLOIDS OR COMPOUNDS THEREOF NOT COVERED BY SUBCLASS C01C
- C01B17/00—Sulfur; Compounds thereof
- C01B17/69—Sulfur trioxide; Sulfuric acid
- C01B17/90—Separation; Purification
- C01B17/901—Recovery from spent acids containing metallic ions, e.g. hydrolysis acids, pickling acids
-
- C—CHEMISTRY; METALLURGY
- C01—INORGANIC CHEMISTRY
- C01G—COMPOUNDS CONTAINING METALS NOT COVERED BY SUBCLASSES C01D OR C01F
- C01G49/00—Compounds of iron
- C01G49/14—Sulfates
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B34/00—Obtaining refractory metals
- C22B34/20—Obtaining niobium, tantalum or vanadium
- C22B34/22—Obtaining vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B47/00—Obtaining manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B59/00—Obtaining rare earth metals
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P20/00—Technologies relating to chemical industry
- Y02P20/10—Process efficiency
- Y02P20/129—Energy recovery, e.g. by cogeneration, H2recovery or pressure recovery turbines
Definitions
- the present disclosure relates to the technical field of resource recovery, and specifically relates to a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production.
- a mainstream production process of titanium dioxide in China is the sulfuric acid method.
- 1 t of TiO 2 produced can generate 6 t to 8 t of waste acid, which has an acid concentration of 18% to 30% and includes ferrous sulfate with a concentration of 8% to 17% as well as a certain amount of the TiO 2 and metal sulfates in addition to H 2 SO 4 .
- Direct neutralization of the waste acid not only wastes a large amount of resources, but also produces a large amount of red gypsum to be stored in landfills and high-salt wastewater to be discharged, causing secondary pollution of the water environment. Therefore, the direct neutralization cannot truly solve environmental problems. As a result, it has always been a technical problem facing titanium dioxide production workers and environmental protection workers to effectively recycle this type of waste acid.
- the waste acid in titanium dioxide production is mainly treated by single evaporation and concentration in China. Specifically, the waste acid is directly evaporated and concentrated to 45% to 70%, compounded with concentrated sulfuric acid, and then returned to the ilmenite leaching section to realize the recovery of acid components.
- this process may produce ferrous sulfate monohydrate with high impurity content and viscosity, and disposal of this type of low-quality ferrous sulfate monohydrate is also a headache faced by enterprises.
- the single evaporation and concentration only recovers sulfuric acid, causing the ferrous sulfate to be lost as a waste, and requires extremely high energy consumption.
- ferrous sulfate One of the raw materials for preparing a battery precursor ferric phosphate is ferrous sulfate, such that there is an increasing demand for ferrous sulfate in the market.
- ferrous sulfate was only an impurity that needed to be removed, and effective recovery was not taken seriously. Accordingly, it is bound to bring great economic and environmental benefits to enterprises and reduce huge burdens by seeking a technical means that can simultaneously recycle ferrous sulfate and sulfuric acid while saving a large amount of steam efficiency.
- Patent CN105439105A disclosed a method of recycling waste acid in titanium dioxide production using a solid-liquid membrane separation + freezing crystallization + nanofiltration membrane separation process, to recover metatitanic acid, ferrous sulfate, and 70% of finished sulfuric acid. Although the process recycles various products, only partial recovery is completed; while a nanofiltration concentrate, which accounts for 25% to 35% of an original waste acid volume, does not undergo resource disposal. Based on the engineering application experience and experimental data of freezing crystallization and the proficient application of nanofiltration membrane technology, the process has a recovery rate on the ferrous sulfate of less than 70%.
- Patent CN111517397A disclosed a three-stage negative-pressure evaporation and crystallization process.
- the process adopts a staged treatment of waste acid, including: conducting freezing crystallization to obtain ferrous sulfate heptahydrate, conducting double-effect evaporation and concentration + freezing crystallization to obtain metal sulfate crystals, and then subjecting secondary freezing crystallization mother liquor to single-effect evaporation and concentration + freezing crystallization to obtain metal sulfate crystals and 70% of finished acid.
- This process is intended to overcome the heater clogging during waste acid concentration. Based on the experiences from freezing crystallization of titanium liquid and concentration of waste acid in titanium dioxide production for ages, this process shows the following three shortcomings.
- the three-stage repeated process from high temperature to low temperature is bound to consume extremely high energy.
- the segmented partial removal of calcium, magnesium, and iron may inevitably lead to the heater clogging.
- CN102910594 discloses a method for recycling iron (II) sulfate and sulfuric acid from waste acid TiO2 production by using heat from the TiO2 roaster.
- the recycling method comprises the following steps: applying water absorbing agent under room temperature and normal pressure under stirring to the waste acid including ferrous sulfate/magnesium sulfate/manganese sulfate and controlling the temperature at 40°C-60°C; cooling the suspension to room temperature, separating the water hydrate crystals by solid-liquid separation, which is a heat exchanger and obtaining a filtrate having a higher sulphuric acid concentration; the filtrate is subjected to freezing to -5°C to 10°C, so that the ferrous sulfate heptahydrate is precipitated in the solution and the solid solution of the ferrous sulfate heptahydrate is separated by solid-liquid separation and the spent acid is further concentrated; these steps might be repeated until the concentration of the sulfuric acid reaches 60 % by mass; exhaust
- the filter cake comprises Ti, Mn,Mg and is further recovered; the sulfuric acid is sent to the acid hydrolysis step for recycling.
- the waste heat of the calcining furnace is obtained after the hot gas of the rotary kiln head and kiln tail is removed from the cyclone separator.
- An objective of the present disclosure is to provide a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production.
- the method saves energy consumption, has a high system recovery rate of ferrous sulfate and a high purity of ferrous sulfate heptahydrate, and can provide a finished acid with a concentration that meets the demand.
- the objective of the present disclosure is achieved as follows:
- the present disclosure provides a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production, including the following steps:
- the waste acid in titanium dioxide production is at least one selected from the group consisting of a waste acid produced after high-pressure filtration of hydrolyzed metatitanic acid, a waste acid produced after adiabatic flash and the high-pressure filtration of the hydrolyzed metatitanic acid, and a waste acid produced after direct filtration of the hydrolyzed metatitanic acid on blades of a leaf filter; and the waste acid in titanium dioxide production has an acid concentration of 20.38% to 25.05% and a ferrous sulfate concentration of 12.25% to 15.33% in step 1.
- a rotary kiln flue gas is at 300°C to 450°C, and the waste acid in titanium dioxide production pre-concentrated by the rotary kiln flue gas spraying is at 75°C to 85°C in step 1.
- a device for the freezing crystallization includes the heat exchanger, a refrigeration unit, a crystallization tank, a centrifuge or a disc filter, a pump unit, and a tank body; and a cold source for the freezing crystallization includes a crystallization completion liquid of 0°C to 10°C and a water chilling unit in step 2.
- the freezing crystallization is conducted at 2°C to 12°C for 0.5 h to 3 h; the ferrous sulfate heptahydrate has a grade of 80.2% to 87.8%; and the crystallization mother liquor has an acid concentration increased to 29.91% to 45.91% in step 2.
- the waste acid evaporation system in step 3 has a concentration device provided with a preheater, a heater, a cooler, a condenser, an evaporator, a maturation cooling tank, a pump unit, and a tank body, and a heat source for evaporation is waste heat derived from a primary steam, a tail gas of titanium dioxide calcination, or a tail gas of acid hydrolysis; and the filter press dehydration system in step 4 is a filtration device being one selected from the group consisting of a membrane filter press, a centrifuge, and a belt filter press combined with supporting facilities thereof.
- the waste acid evaporation system has an effective number of 1 to 3; and the evaporation condensed water has an acid concentration of less than 0.5%.
- the precipitated miscellaneous salt-containing suspended concentrated acid has an acid concentration of 50% to 85%.
- the filtered finished acid obtained in step 4 is pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain a ferrous sulfate heptahydrate crystal; a resulting freezing crystallization mother liquor is collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflows to a maturation cooling tank to allow standing for approximately 10 h, and is then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
- the present disclosure combines the waste heat from a large amount of high-temperature rotary kiln exhaust gas produced by titanium dioxide enterprises, the high-quality ferrous sulfate heptahydrate obtained by freezing crystallization, and the solubility of ferrous sulfate in a sulfuric acid system.
- the present disclosure proposes a relatively-single multi-effect evaporation and concentration method for a waste acid in titanium dioxide production that contains high concentrations of ferrous sulfate and sulfuric acid. The method can save energy consumption by not less than 50%, and simultaneously recover the ferrous sulfate with high system recovery rate, ferrous sulfate heptahydrate with high purity, and finished acid with a concentration that meets customer demands.
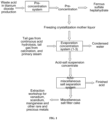
- FIG. 1 shows a schematic diagram of a working flow in the present disclosure.
- the present disclosure provides a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production, including the following steps:
- the waste acid in titanium dioxide production is at least one selected from the group consisting of a waste acid produced after high-pressure filtration of hydrolyzed metatitanic acid, a waste acid produced after adiabatic flash and the high-pressure filtration of the hydrolyzed metatitanic acid, and a waste acid produced after direct filtration of the hydrolyzed metatitanic acid on blades of a leaf filter; and the waste acid in titanium dioxide production has an acid concentration of 20.38% to 25.05% and a ferrous sulfate concentration of 12.25% to 15.33% in step 1.
- the pre-concentrating is conducted by rotary kiln flue gas spraying, the rotary kiln flue gas spraying in series with flash evaporation, or a combination of the flash evaporation, the rotary kiln flue gas spraying, and the flash evaporation in sequence; and the rotary kiln flue gas spraying concentrates the waste acid in titanium dioxide production to 27.86% to 29.4%.
- a rotary kiln flue gas is at 300°C to 450°C, and the waste acid in titanium dioxide production pre-concentrated by the rotary kiln flue gas spraying is at 75°C to 85°C in step 1.
- a device for the freezing crystallization includes the heat exchanger, a refrigeration unit, a crystallization tank, a centrifuge or a disc filter, a pump unit, and a tank body; and a cold source for the freezing crystallization includes a crystallization completion liquid of 0°C to 10°C and a water chilling unit in step 2.
- the freezing crystallization is conducted at 2°C to 12°C for 0.5 h to 3 h; the ferrous sulfate heptahydrate has a grade of 80.2% to 87.8%; and the crystallization mother liquor has an acid concentration increased to 29.91% to 45.91% in step 2.
- the waste acid evaporation system in step 3 has a concentration device provided with a preheater, a heater, a cooler, a condenser, an evaporator, a maturation cooling tank, a pump unit, and a tank body, and a heat source for evaporation is waste heat derived from a primary steam, a tail gas of titanium dioxide calcination, or a tail gas of acid hydrolysis; and the filter press dehydration system in step 4 is a filtration device being one selected from the group consisting of a membrane filter press, a centrifuge, and a belt filter press combined with supporting facilities thereof.
- the waste acid evaporation system has an effective number of 1 to 3; and the evaporation condensed water has an acid concentration of less than 0.5%.
- the precipitated miscellaneous salt-containing suspended concentrated acid has an acid concentration of 50% to 85%.
- the filtered finished acid obtained in step 4 is pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain a ferrous sulfate heptahydrate crystal; a resulting freezing crystallization mother liquor is collected into an evaporation feed tank and pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflows to a maturation cooling tank to allow standing for approximately 10 h, and is then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
- a waste acid in titanium dioxide production had an acid concentration of 22.5%, a ferrous sulfate content of 12.66%, and an SS content of 100 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 400°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 29.4% and a ferrous sulfate concentration of 16.71%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 5°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 86.2% and a recovery rate on ferrous sulfate of 90.3% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 40.3% and a ferrous sulfate concentration of 2.5%; the freezing crystallization mother liquor was collected into an e
- a waste acid in titanium dioxide production had an acid concentration of 24.13%, a ferrous sulfate content of 15.11%, and an SS content of 112 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 50°C with an acid concentration increased to 30.1% and a ferrous sulfate concentration of 19.44%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 5°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.6% and a recovery rate on ferrous sulfate of 92% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 45.91% and a ferrous sulfate concentration of 2.22%; the freezing crystallization mother liquor was collected into an
- Example 3 A waste acid in titanium dioxide production had an acid concentration of 24.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 29.85% and a ferrous sulfate concentration of 16.56%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 12°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 85.2% and a recovery rate on ferrous sulfate of 73.22% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 37.51% and a ferrous sulfate concentration of 6.02%;
- a filtrate with an acid concentration of 37.51% was pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.5% and a secondary recovery rate on ferrous sulfate of 73.86% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 40.14% and a ferrous sulfate concentration of 1.68%; the freezing crystallization mother liquor was collected into an evaporation feed tank and pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
- the ferrous sulfate had a total recovery rate of 93.23%.
- a waste acid in titanium dioxide production had an acid concentration of 25.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 75°C with an acid concentration increased to 29.91% and a ferrous sulfate concentration of 16.12%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 15°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.8% and a recovery rate on ferrous sulfate of 58.20% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 36.59% and a ferrous sulfate concentration of 8.73%; the freezing crystallization mother liquor was collected
- a waste acid in titanium dioxide production had an acid concentration of 24.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 50°C with an acid concentration increased to 31.85% and a ferrous sulfate concentration of 18.25%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 10°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 80.2% and a recovery rate on ferrous sulfate of 73.58% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 42.20% and a ferrous sulfate concentration of 5.92%; the freezing crystallization mother liquor was collected into an
- a waste acid in titanium dioxide production had an acid concentration of 20.38%, a ferrous sulfate content of 12.25%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 27.86% and a ferrous sulfate concentration of 16.72%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 2°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 86.8% and a recovery rate on ferrous sulfate of 91.03% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 38.63% and a ferrous sulfate concentration of 2.02%; the freezing crystallization mother liquor was collected into
- Example 1 The minimum recovery rates of ferrous sulfate in Example 1 to Example 5 reached averagely not less than 70%: Table 1 Experimental data of direct freezing crystallization Experimental SN Process Sample H 2 SO 4 content FeSO 4 content FeSO 4 recovery rate 1 Freezing crystallization Pre-concentrated acid 22.5% 12.66% - Freezing crystallization mother liquor 26.4% 5.32% - Crystal - - 64.2% 2 Freezing crystallization Pre-concentrated acid 23.1% 15.11% - Freezing crystallization mother liquor 28.6% 5.67% - Crystal - - 69.7% Table 2 Experimental data of "pre-concentration + freezing crystallization" Experimenta l SN Process Sample H 2 SO 4 content FeSO 4 content FeSO 4 ⁇ 7H 2 O FeSO 4 recover y rate Example 1 Pre-concentratio n Waste acid in titanium dioxide production 22.5% 12.66 % - - Pre-concentrate d acid 29.4% 16.71 % - - Freezing crystallization Pre-concentrate d acid 29.4% 16.
Landscapes
- Chemical & Material Sciences (AREA)
- Organic Chemistry (AREA)
- Inorganic Chemistry (AREA)
- Inorganic Compounds Of Heavy Metals (AREA)
- Organic Low-Molecular-Weight Compounds And Preparation Thereof (AREA)
- Removal Of Specific Substances (AREA)
- Manufacture And Refinement Of Metals (AREA)
- Vaporization, Distillation, Condensation, Sublimation, And Cold Traps (AREA)
Description
- The present disclosure relates to the technical field of resource recovery, and specifically relates to a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production.
- A mainstream production process of titanium dioxide in China is the sulfuric acid method. 1 t of TiO2 produced can generate 6 t to 8 t of waste acid, which has an acid concentration of 18% to 30% and includes ferrous sulfate with a concentration of 8% to 17% as well as a certain amount of the TiO2 and metal sulfates in addition to H2SO4. Direct neutralization of the waste acid not only wastes a large amount of resources, but also produces a large amount of red gypsum to be stored in landfills and high-salt wastewater to be discharged, causing secondary pollution of the water environment. Therefore, the direct neutralization cannot truly solve environmental problems. As a result, it has always been a technical problem facing titanium dioxide production workers and environmental protection workers to effectively recycle this type of waste acid.
- The waste acid in titanium dioxide production is mainly treated by single evaporation and concentration in China. Specifically, the waste acid is directly evaporated and concentrated to 45% to 70%, compounded with concentrated sulfuric acid, and then returned to the ilmenite leaching section to realize the recovery of acid components. However, this process may produce ferrous sulfate monohydrate with high impurity content and viscosity, and disposal of this type of low-quality ferrous sulfate monohydrate is also a headache faced by enterprises. The single evaporation and concentration only recovers sulfuric acid, causing the ferrous sulfate to be lost as a waste, and requires extremely high energy consumption. In recent years, with the rapid rise of domestic new energy vehicles, lithium iron phosphate has become one of the main materials for battery cathodes. One of the raw materials for preparing a battery precursor ferric phosphate is ferrous sulfate, such that there is an increasing demand for ferrous sulfate in the market. In the past, the ferrous sulfate was only an impurity that needed to be removed, and effective recovery was not taken seriously. Accordingly, it is bound to bring great economic and environmental benefits to enterprises and reduce huge burdens by seeking a technical means that can simultaneously recycle ferrous sulfate and sulfuric acid while saving a large amount of steam efficiency.
- Patent
CN105439105A disclosed a method of recycling waste acid in titanium dioxide production using a solid-liquid membrane separation + freezing crystallization + nanofiltration membrane separation process, to recover metatitanic acid, ferrous sulfate, and 70% of finished sulfuric acid. Although the process recycles various products, only partial recovery is completed; while a nanofiltration concentrate, which accounts for 25% to 35% of an original waste acid volume, does not undergo resource disposal. Based on the engineering application experience and experimental data of freezing crystallization and the proficient application of nanofiltration membrane technology, the process has a recovery rate on the ferrous sulfate of less than 70%. - Patent
CN111517397A disclosed a three-stage negative-pressure evaporation and crystallization process. The process adopts a staged treatment of waste acid, including: conducting freezing crystallization to obtain ferrous sulfate heptahydrate, conducting double-effect evaporation and concentration + freezing crystallization to obtain metal sulfate crystals, and then subjecting secondary freezing crystallization mother liquor to single-effect evaporation and concentration + freezing crystallization to obtain metal sulfate crystals and 70% of finished acid. This process is intended to overcome the heater clogging during waste acid concentration. Based on the experiences from freezing crystallization of titanium liquid and concentration of waste acid in titanium dioxide production for ages, this process shows the following three shortcomings. On one hand, the three-stage repeated process from high temperature to low temperature is bound to consume extremely high energy. On the other hand, the segmented partial removal of calcium, magnesium, and iron may inevitably lead to the heater clogging. Furthermore, there is a recovery rate on the ferrous sulfate of less than 60%, and the second and third stages of concentration and crystallization mainly produce miscellaneous metal sulfates. -
CN102910594 discloses a method for recycling iron (II) sulfate and sulfuric acid from waste acid TiO2 production by using heat from the TiO2 roaster. The recycling method comprises the following steps: applying water absorbing agent under room temperature and normal pressure under stirring to the waste acid including ferrous sulfate/magnesium sulfate/manganese sulfate and controlling the temperature at 40°C-60°C; cooling the suspension to room temperature, separating the water hydrate crystals by solid-liquid separation, which is a heat exchanger and obtaining a filtrate having a higher sulphuric acid concentration; the filtrate is subjected to freezing to -5°C to 10°C, so that the ferrous sulfate heptahydrate is precipitated in the solution and the solid solution of the ferrous sulfate heptahydrate is separated by solid-liquid separation and the spent acid is further concentrated; these steps might be repeated until the concentration of the sulfuric acid reaches 60 % by mass; exhaust gas of the roasting furnace is used to heat and dehydrated the water absorbing agent hydrate to regenerate the water absorbing agent; the water vapour is cooled by the room temperature waste acid partition wall and returned to the pickling process to be used for the titanium acid washing water. The filter cake comprises Ti, Mn,Mg and is further recovered; the sulfuric acid is sent to the acid hydrolysis step for recycling. The waste heat of the calcining furnace is obtained after the hot gas of the rotary kiln head and kiln tail is removed from the cyclone separator. - An objective of the present disclosure is to provide a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production. The method saves energy consumption, has a high system recovery rate of ferrous sulfate and a high purity of ferrous sulfate heptahydrate, and can provide a finished acid with a concentration that meets the demand.
- The objective of the present disclosure is achieved as follows: The present disclosure provides a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production, including the following steps:
- step 1: pre-concentrating the waste acid in titanium dioxide production to obtain a pre-concentrated acid;
- step 2: cooling the pre-concentrated acid by a heat exchanger, and conducting freezing crystallization for a period of time to obtain the ferrous sulfate heptahydrate and a crystallization mother liquor;
- step 3: concentrating the crystallization mother liquor in a waste acid evaporation system to obtain precipitated miscellaneous salt-containing suspended concentrated acid and evaporation condensed water; and
- step 4: subjecting the precipitated miscellaneous salt-containing suspended concentrated acid to maturing and cooling, and then transferring a resulting product into a filter press dehydration system to allow a treatment to obtain a metal miscellaneous salt filter cake and a filtered finished acid; where the metal miscellaneous salt filter cake serves as a raw material for extracting precious metals including titanium, manganese, magnesium, scandium, and vanadium as well as iron to allow resource recovery, and the filtered finished acid is returned to an ilmenite acid hydrolysis section;
- wherein in step 1, the pre-concentrating is conducted by rotary kiln flue gas spraying, the rotary kiln flue gas spraying in series with flash evaporation, or a combination of the flash evaporation, the rotary kiln flue gas spraying, and the flash evaporation in sequence; and the rotary kiln flue gas spraying concentrates the waste acid in titanium dioxide production to 27.86% to 29.4%.
- In the present disclosure, the waste acid in titanium dioxide production is at least one selected from the group consisting of a waste acid produced after high-pressure filtration of hydrolyzed metatitanic acid, a waste acid produced after adiabatic flash and the high-pressure filtration of the hydrolyzed metatitanic acid, and a waste acid produced after direct filtration of the hydrolyzed metatitanic acid on blades of a leaf filter; and the waste acid in titanium dioxide production has an acid concentration of 20.38% to 25.05% and a ferrous sulfate concentration of 12.25% to 15.33% in step 1.
- In the present disclosure, a rotary kiln flue gas is at 300°C to 450°C, and the waste acid in titanium dioxide production pre-concentrated by the rotary kiln flue gas spraying is at 75°C to 85°C in step 1.
- In the present disclosure, a device for the freezing crystallization includes the heat exchanger, a refrigeration unit, a crystallization tank, a centrifuge or a disc filter, a pump unit, and a tank body; and a cold source for the freezing crystallization includes a crystallization completion liquid of 0°C to 10°C and a water chilling unit in step 2.
- In the present disclosure, the freezing crystallization is conducted at 2°C to 12°C for 0.5 h to 3 h; the ferrous sulfate heptahydrate has a grade of 80.2% to 87.8%; and the crystallization mother liquor has an acid concentration increased to 29.91% to 45.91% in step 2.
- In the present disclosure, the waste acid evaporation system in step 3 has a concentration device provided with a preheater, a heater, a cooler, a condenser, an evaporator, a maturation cooling tank, a pump unit, and a tank body, and a heat source for evaporation is waste heat derived from a primary steam, a tail gas of titanium dioxide calcination, or a tail gas of acid hydrolysis; and the filter press dehydration system in step 4 is a filtration device being one selected from the group consisting of a membrane filter press, a centrifuge, and a belt filter press combined with supporting facilities thereof.
- In the present disclosure, the waste acid evaporation system has an effective number of 1 to 3; and the evaporation condensed water has an acid concentration of less than 0.5%.
- In the present disclosure, the precipitated miscellaneous salt-containing suspended concentrated acid has an acid concentration of 50% to 85%.
- In the present disclosure, the filtered finished acid obtained in step 4 is pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain a ferrous sulfate heptahydrate crystal; a resulting freezing crystallization mother liquor is collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflows to a maturation cooling tank to allow standing for approximately 10 h, and is then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
- The present disclosure combines the waste heat from a large amount of high-temperature rotary kiln exhaust gas produced by titanium dioxide enterprises, the high-quality ferrous sulfate heptahydrate obtained by freezing crystallization, and the solubility of ferrous sulfate in a sulfuric acid system. The present disclosure proposes a relatively-single multi-effect evaporation and concentration method for a waste acid in titanium dioxide production that contains high concentrations of ferrous sulfate and sulfuric acid. The method can save energy consumption by not less than 50%, and simultaneously recover the ferrous sulfate with high system recovery rate, ferrous sulfate heptahydrate with high purity, and finished acid with a concentration that meets customer demands.
- The present disclosure also has the following advantages:
- 1. The process of "pre-concentrating the waste acid in titanium dioxide production and then conducting freezing crystallization" is better than the process of "conducting freezing crystallization, and then transferring to kiln tail gas for concentration". Since the acid concentration and the ferrous sulfate concentration are both increased, according to a rule "the greater the acid concentration, the lower the solubility of ferrous sulfate", favorable conditions are created for subsequent freezing crystallization to obtain ferrous sulfate with the high recovery rate and high grade.
- 2. Pre-concentration and/or flash evaporation of the rotary kiln tail gas removes part of water, and there is the high recovery rate of ferrous sulfate as mentioned in Advantage 1, such that more ferrous sulfate heptahydrate is precipitated for taking away more iron salts and moisture, thus further increasing the acid concentration. Finally, the acid entering the waste acid concentration system has a concentration starting point that reaches a high value, thereby minimizing the amount of evaporated water required by the subsequent waste acid evaporation and concentration device and saves steam consumption.
- 3. In the present disclosure, the ferrous sulfate heptahydrate with high purity and high recovery rate and finished acid that meets customer demands can be obtained simultaneously. In addition, a metal miscellaneous salt-enriched filter cake with low ferrous sulfate content can also be obtained separately, and is used for the comprehensive utilization of rare and precious metals such as vanadium, scandium, and manganese.
- 4. In the present disclosure, the emission of gypsum slag is reduced while recycling ferrous sulfate and waste acid by more than 90% on the original basis, thereby achieving near-zero emission of gypsum slag produced by the sulfuric acid method from titanium dioxide.
- The present disclosure is described in more detail hereinafter with reference to the accompanying drawings and specific embodiments.
-
FIG. 1 shows a schematic diagram of a working flow in the present disclosure. - The examples of the present disclosure are described in detail below with reference to the drawings.
- The present disclosure provides a method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production, including the following steps:
- step 1: pre-concentrating the waste acid in titanium dioxide production to obtain a pre-concentrated acid;
- step 2: cooling the pre-concentrated acid by a heat exchanger, and conducting freezing crystallization for a period of time to obtain the ferrous sulfate heptahydrate and a crystallization mother liquor;
- step 3: concentrating the crystallization mother liquor in a waste acid evaporation system to obtain precipitated miscellaneous salt-containing suspended concentrated acid and evaporation condensed water; and
- step 4: subjecting the precipitated miscellaneous salt-containing suspended concentrated acid to maturing and cooling, and then transferring a resulting product into a filter press dehydration system to allow a treatment to obtain a metal miscellaneous salt filter cake and a filtered finished acid; where the metal miscellaneous salt filter cake serves as a raw material for extracting precious metals including titanium, manganese, magnesium, scandium, and vanadium as well as iron to allow resource recovery, and the filtered finished acid is returned to an ilmenite acid hydrolysis section.
- In the present disclosure, the waste acid in titanium dioxide production is at least one selected from the group consisting of a waste acid produced after high-pressure filtration of hydrolyzed metatitanic acid, a waste acid produced after adiabatic flash and the high-pressure filtration of the hydrolyzed metatitanic acid, and a waste acid produced after direct filtration of the hydrolyzed metatitanic acid on blades of a leaf filter; and the waste acid in titanium dioxide production has an acid concentration of 20.38% to 25.05% and a ferrous sulfate concentration of 12.25% to 15.33% in step 1.
- In the present disclosure, the pre-concentrating is conducted by rotary kiln flue gas spraying, the rotary kiln flue gas spraying in series with flash evaporation, or a combination of the flash evaporation, the rotary kiln flue gas spraying, and the flash evaporation in sequence; and the rotary kiln flue gas spraying concentrates the waste acid in titanium dioxide production to 27.86% to 29.4%.
- In the present disclosure, a rotary kiln flue gas is at 300°C to 450°C, and the waste acid in titanium dioxide production pre-concentrated by the rotary kiln flue gas spraying is at 75°C to 85°C in step 1.
- In the present disclosure, a device for the freezing crystallization includes the heat exchanger, a refrigeration unit, a crystallization tank, a centrifuge or a disc filter, a pump unit, and a tank body; and a cold source for the freezing crystallization includes a crystallization completion liquid of 0°C to 10°C and a water chilling unit in step 2.
- In the present disclosure, the freezing crystallization is conducted at 2°C to 12°C for 0.5 h to 3 h; the ferrous sulfate heptahydrate has a grade of 80.2% to 87.8%; and the crystallization mother liquor has an acid concentration increased to 29.91% to 45.91% in step 2.
- In the present disclosure, the waste acid evaporation system in step 3 has a concentration device provided with a preheater, a heater, a cooler, a condenser, an evaporator, a maturation cooling tank, a pump unit, and a tank body, and a heat source for evaporation is waste heat derived from a primary steam, a tail gas of titanium dioxide calcination, or a tail gas of acid hydrolysis; and the filter press dehydration system in step 4 is a filtration device being one selected from the group consisting of a membrane filter press, a centrifuge, and a belt filter press combined with supporting facilities thereof.
- In the present disclosure, the waste acid evaporation system has an effective number of 1 to 3; and the evaporation condensed water has an acid concentration of less than 0.5%.
- In the present disclosure, the precipitated miscellaneous salt-containing suspended concentrated acid has an acid concentration of 50% to 85%.
- In the present disclosure, the filtered finished acid obtained in step 4 is pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain a ferrous sulfate heptahydrate crystal; a resulting freezing crystallization mother liquor is collected into an evaporation feed tank and pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflows to a maturation cooling tank to allow standing for approximately 10 h, and is then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
- A waste acid in titanium dioxide production had an acid concentration of 22.5%, a ferrous sulfate content of 12.66%, and an SS content of 100 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 400°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 29.4% and a ferrous sulfate concentration of 16.71%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 5°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 86.2% and a recovery rate on ferrous sulfate of 90.3% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 40.3% and a ferrous sulfate concentration of 2.5%; the freezing crystallization mother liquor was collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 11 h, and was then pumped by a screw into a membrane filter press to obtain 82% of a finished acid and a metal miscellaneous salt filter cake.
- A waste acid in titanium dioxide production had an acid concentration of 24.13%, a ferrous sulfate content of 15.11%, and an SS content of 112 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 50°C with an acid concentration increased to 30.1% and a ferrous sulfate concentration of 19.44%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 5°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.6% and a recovery rate on ferrous sulfate of 92% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 45.91% and a ferrous sulfate concentration of 2.22%; the freezing crystallization mother liquor was collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped by a screw into a membrane filter press to obtain 75% of a finished acid and a metal miscellaneous salt filter cake.
- Example 3: A waste acid in titanium dioxide production had an acid concentration of 24.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 29.85% and a ferrous sulfate concentration of 16.56%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 12°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 85.2% and a recovery rate on ferrous sulfate of 73.22% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 37.51% and a ferrous sulfate concentration of 6.02%;
- further, a filtrate with an acid concentration of 37.51% was pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.5% and a secondary recovery rate on ferrous sulfate of 73.86% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 40.14% and a ferrous sulfate concentration of 1.68%; the freezing crystallization mother liquor was collected into an evaporation feed tank and pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake. The ferrous sulfate had a total recovery rate of 93.23%.
- A waste acid in titanium dioxide production had an acid concentration of 25.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 75°C with an acid concentration increased to 29.91% and a ferrous sulfate concentration of 16.12%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 15°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 87.8% and a recovery rate on ferrous sulfate of 58.20% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 36.59% and a ferrous sulfate concentration of 8.73%; the freezing crystallization mother liquor was collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped by a screw into a membrane filter press to obtain 68.2% of a finished acid and a metal miscellaneous salt filter cake.
- A waste acid in titanium dioxide production had an acid concentration of 24.05%, a ferrous sulfate content of 13.78%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 50°C with an acid concentration increased to 31.85% and a ferrous sulfate concentration of 18.25%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 10°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 80.2% and a recovery rate on ferrous sulfate of 73.58% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 42.20% and a ferrous sulfate concentration of 5.92%; the freezing crystallization mother liquor was collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped by a screw into a membrane filter press to obtain 72% of a finished acid and a metal miscellaneous salt filter cake.
- A waste acid in titanium dioxide production had an acid concentration of 20.38%, a ferrous sulfate content of 12.25%, and an SS content of 102 mg/L; the waste acid in titanium dioxide production was pumped to a Venturi tower to allow direct-contact heat exchange, evaporation, and pre-concentration with a 360°C rotary kiln tail gas, to obtain a pre-concentrated acid at 80°C with an acid concentration increased to 27.86% and a ferrous sulfate concentration of 16.72%; the pre-concentrated acid was then pumped into a freezing crystallization system to allow freezing crystallization at 2°C for 2.0 h to obtain ferrous sulfate heptahydrate crystals with a grade of 86.8% and a recovery rate on ferrous sulfate of 91.03% after sampling detection; while a resulting freezing crystallization mother liquor had an acid concentration of 38.63% and a ferrous sulfate concentration of 2.02%; the freezing crystallization mother liquor was collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; the acid-salt suspension concentrate overflowed to a maturation cooling tank to allow standing for approximately 10 h, and was then pumped by a screw into a membrane filter press to obtain 88.2% of a finished acid and a metal miscellaneous salt filter cake.
- The specific effect data of the examples were shown in Table 2.
- Samples of the waste acid in titanium dioxide production were collected from two different manufacturers. In order to find out the of low recovery rate of ferrous sulfate in the methods of direct freezing crystallization of waste acid in titanium dioxide production to obtain ferrous sulfate heptahydrate of Patents
CN105439105A andCN111517397A , the direct freezing crystallization of waste acid in titanium dioxide production to obtain ferrous sulfate heptahydrate was simulated. Two sets of parallel experimental data were shown in Table 1, and recovery rates of ferrous sulfate were both less than 70%. In order to demonstrate the advancement of the present disclosure, the "pre-concentration + freezing crystallization" process of waste acid in titanium dioxide production was simulated, and two sets of parallel experimental data were shown in Table 2. The minimum recovery rates of ferrous sulfate in Example 1 to Example 5 reached averagely not less than 70%:Table 1 Experimental data of direct freezing crystallization Experimental SN Process Sample H2SO4 content FeSO4 content FeSO4 recovery rate 1 Freezing crystallization Pre-concentrated acid 22.5% 12.66% - Freezing crystallization mother liquor 26.4% 5.32% - Crystal - - 64.2% 2 Freezing crystallization Pre-concentrated acid 23.1% 15.11% - Freezing crystallization mother liquor 28.6% 5.67% - Crystal - - 69.7% Table 2 Experimental data of "pre-concentration + freezing crystallization" Experimenta l SN Process Sample H2SO4 content FeSO4 content FeSO4·7H2 O FeSO4 recover y rate Example 1 Pre-concentratio n Waste acid in titanium dioxide production 22.5% 12.66 % - - Pre-concentrate d acid 29.4% 16.71 % - - Freezing crystallization Pre-concentrate d acid 29.4% 16.71 % - - Freezing crystallization mother liquor 40.3% 2.5% - - Crystal - - 86.2% 90.3% Example 2 Pre-concentratio n Waste acid in titanium dioxide production 24.13 % 15.33 % - - Pre-concentrate d waste acid 30.6% 19.44 % - - Freezing crystallization Pre-concentrate d acid 30.6% 19.44 % - - Freezing crystallization mother liquor 45.91 % 2.22% - - crystal - - 87.8% 92% Example 3 Pre-concentratio n Waste acid in titanium dioxide production 24.05 % 13.78 % - - Pre-concentrate d acid 28.85 % 16.56 % - - Freezing crystallization Pre-concentrate d acid 28.85 % 16.56 % - - Freezing crystallization mother liquor 37.51 % 6.02% - - Crystal - - 85.2% 73.22% Secondary freezing crystallization mother liquor 40.14 % 1.68% Secondary crystal - 87.5% 73.86% Total recovery rate - 93.23% Example 4 Pre-concentratio n Waste acid in titanium dioxide production 25.05 % 13.78 % - - Pre-concentrate d acid 29.91 % 16.12 % - - Freezing crystallization Pre-concentrate d acid 29.91 % 16.12 % - - Freezing crystallization mother liquor 36.59 % 8.73% - - crystal - - 87.8% 58.2% Example 5 Pre-concentratio n Waste acid in titanium dioxide production 24.05 % 13.78 % - - Pre-concentrate d acid 31.85 % 18.25 % - - Freezing crystallization Pre-concentrate d acid 31.85 % 18.25 % - - Freezing crystallization mother liquor 42.20 % 5.92% - - crystal - - 80.2% 73.58% Example 6 Pre-concentratio n Waste acid in titanium dioxide production 20.38 % 12.25 % - - Pre-concentrate d acid 27.86 % 16.72 % - - Freezing crystallization Pre-concentrate d acid 27.86 % 16.72 % - - Freezing crystallization mother liquor 38.63 % 2.02% - - Crystal - - 86.8% 91.03% - The present disclosure may have the following advantages:
- 1. The process of "pre-concentrating the waste acid in titanium dioxide production and then conducting freezing crystallization" is better than the process of "conducting freezing crystallization, and then transferring to kiln tail gas for concentration". Since the acid concentration and the ferrous sulfate concentration are both increased, according to a rule "the greater the acid concentration, the lower the solubility of ferrous sulfate", favorable conditions are created for subsequent freezing crystallization to obtain ferrous sulfate with the high recovery rate and high grade.
- 2. Pre-concentration and/or flash evaporation of the rotary kiln tail gas removes part of water, and there is the high recovery rate of ferrous sulfate as mentioned in Advantage 1, such that more ferrous sulfate heptahydrate is precipitated for taking away more iron salts and moisture, thus further increasing the acid concentration. Finally, the acid entering the waste acid concentration system has a concentration starting point that reaches a high value, thereby minimizing the amount of evaporated water required by the subsequent waste acid evaporation and concentration device and saves steam consumption.
- 3. In the present disclosure, the ferrous sulfate heptahydrate with high purity and high recovery rate and finished acid that meets customer demands can be obtained simultaneously. In addition, a metal miscellaneous salt-enriched filter cake with low ferrous sulfate content can also be obtained separately, and is used for the comprehensive utilization of rare and precious metals such as vanadium, scandium, and manganese.
- 4. In the present disclosure, the emission of gypsum slag is reduced while recycling ferrous sulfate and waste acid by more than 90% on the original basis, thereby achieving near-zero emission of gypsum slag produced by the sulfuric acid method from titanium dioxide.
- 5. As shown in Example 1 to 2, when a freezing temperature was 5°C and the waste acid concentration was about 30%, the iron removal rate was above 90%. As shown in Example 3 to 5, the ferrous iron removal rate was about 73% at 10°C to 12°C. When the 10°C freezing crystallization mother liquor was continued to cool to 4°C, the secondary iron removal rate was 73%. After step-by-step cooling, the total iron recovery rate was 93%. That is to say, there was no significant change in the iron recovery rate between one-time cooling and step-by-step cooling, but operating procedures of the crystallization were increased. As shown in Example 4, when the cooling temperature was increased to 15°C, the iron removal rate decreased to not greater than 70%. As shown in Example 6, when the cooling temperature was reduced from 4°C to 2°C, the iron removal rate showed no change, but more work was consumed when the waste acid was reduced from 4°C to 2°C, resulting in increased power consumption. As shown in the above examples, when freezing crystallization was conducted to remove iron from waste acid, the cooling temperature had the greatest impact on the iron removal efficiency, followed by the sulfuric acid concentration in the waste acid, and then the ferrous sulfate content in the starting waste acid.
- The above descriptions are only preferred embodiments of the present disclosure and are not intended to limit the present disclosure.
Claims (9)
- A method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production, comprising the following steps:step 1: pre-concentrating the waste acid in titanium dioxide production to obtain a pre-concentrated acid;step 2: cooling the pre-concentrated acid by a heat exchanger, and conducting freezing crystallization for a period of time to obtain the ferrous sulfate heptahydrate and a crystallization mother liquor;step 3: concentrating the crystallization mother liquor in a waste acid evaporation system to obtain precipitated miscellaneous salt-containing suspended concentrated acid and evaporation condensed water; andstep 4: subjecting the precipitated miscellaneous salt-containing suspended concentrated acid to maturing and cooling, and then transferring a resulting product into a filter press dehydration system to allow a treatment to obtain a metal miscellaneous salt filter cake and a filtered finished acid; wherein the metal miscellaneous salt filter cake serves as a raw material for extracting precious metals comprising titanium, manganese, magnesium, scandium, and vanadium as well as iron to allow resource recovery, and the filtered finished acid is returned to an ilmenite acid hydrolysis section;wherein in step 1, the pre-concentrating is conducted by rotary kiln flue gas spraying, the rotary kiln flue gas spraying in series with flash evaporation, or a combination of the flash evaporation, the rotary kiln flue gas spraying, and the flash evaporation in sequence the rotary kiln flue gas spraying concentrates the waste acid in titanium dioxide production to 27.86% to 29.4%.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1, wherein the waste acid in titanium dioxide production is at least one selected from the group consisting of a waste acid produced after high-pressure filtration of hydrolyzed metatitanic acid, a waste acid produced after adiabatic flash and the high-pressure filtration of the hydrolyzed metatitanic acid, and a waste acid produced after direct filtration of the hydrolyzed metatitanic acid on blades of a leaf filter; and the waste acid in titanium dioxide production has an acid concentration of 20.38% to 25.05% and a ferrous sulfate concentration of 12.25% to 15.33% in step 1.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1, wherein a rotary kiln flue gas is at 300°C to 450°C, and the waste acid in titanium dioxide production pre-concentrated by the rotary kiln flue gas spraying is at 75°C to 85°C in step 1.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein a device for the freezing crystallization comprises the heat exchanger, a refrigeration unit, a crystallization tank, a centrifuge or a disc filter, a pump unit, and a tank body; and a cold source for the freezing crystallization comprises a crystallization completion liquid of 0°C to 10°C and a water chilling unit in step 2.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein the freezing crystallization is conducted at 2°C to 12°C for 0.5 h to 3 h; the ferrous sulfate heptahydrate has a grade of 80.2% to 87.8%; and the crystallization mother liquor has an acid concentration increased to 29.91% to 45.91% in step 2.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein the waste acid evaporation system in step 3 has a concentration device provided with a preheater, a heater, a cooler, a condenser, an evaporator, a maturation cooling tank, a pump unit, and a tank body, and a heat source for evaporation is waste heat derived from a primary steam, a tail gas of titanium dioxide calcination, or a tail gas of acid hydrolysis; and the filter press dehydration system in step 4 is a filtration device being one selected from the group consisting of a membrane filter press, a centrifuge, and a belt filter press combined with supporting facilities thereof.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein the waste acid evaporation system has an effective number of 1 to 3; and the evaporation condensed water has an acid concentration of less than 0.5%.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein the precipitated miscellaneous salt-containing suspended concentrated acid has an acid concentration of 50% to 85%.
- The method for recycling ferrous sulfate heptahydrate and sulfuric acid from a waste acid in titanium dioxide production according to claim 1 or 2, wherein the filtered finished acid obtained in step 4 is pumped into a freezing crystallization system to allow the freezing crystallization at 4°C for 2.0 h to obtain a ferrous sulfate heptahydrate crystal; a resulting freezing crystallization mother liquor is collected into an evaporation feed tank and then pumped into a double-effect evaporation device to obtain an acid-salt suspension concentrate; and the acid-salt suspension concentrate overflows to a maturation cooling tank to allow standing for approximately 10 h, and is then pumped into a membrane filter press through a screw to obtain 85% of a finished acid and the metal miscellaneous salt filter cake.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211598908.8A CN116002768A (en) | 2022-12-14 | 2022-12-14 | A kind of method of recovering ferrous sulfate heptahydrate and sulfuric acid from waste acid of titanium dioxide |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP4389707A1 EP4389707A1 (en) | 2024-06-26 |
| EP4389707C0 EP4389707C0 (en) | 2025-05-28 |
| EP4389707B1 true EP4389707B1 (en) | 2025-05-28 |
Family
ID=86018332
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23216801.3A Active EP4389707B1 (en) | 2022-12-14 | 2023-12-14 | Method for recycling ferrous sulfate heptahydrate and sulfuric acid from waste acid in titanium dioxide production |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4389707B1 (en) |
| CN (1) | CN116002768A (en) |
| ZA (1) | ZA202311407B (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116812984A (en) * | 2023-07-25 | 2023-09-29 | 南通三圣石墨设备科技股份有限公司 | Efficient crystallization method for producing ferrous sulfate heptahydrate from titanium white waste acid |
| CN117339227A (en) * | 2023-09-20 | 2024-01-05 | 龙佰襄阳钛业有限公司 | A kind of concentrated waste acid acid preparation process |
| CN118851468A (en) * | 2024-07-12 | 2024-10-29 | 北京水木智创环保科技有限公司 | A new method for recycling and comprehensive treatment of waste titanium dioxide acid resources |
| CN119240621A (en) * | 2024-11-04 | 2025-01-03 | 浙江明炬环境科技股份有限公司 | A process for recycling waste acid from titanium dioxide produced by sulfuric acid process |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0362428B1 (en) * | 1988-10-06 | 1992-12-23 | KRONOS TITAN-Gesellschaft mbH | Process and apparatus for the treatment of a sulfuric-acid solution containing ferrous sulfate |
| RU2311341C1 (en) * | 2006-05-10 | 2007-11-27 | Юрий Борисович Данилов | Exhausted sulfuric acid regeneration process |
| CN102910594B (en) * | 2012-11-06 | 2014-10-29 | 黄正源 | Method for concentrating waste sulfuric acid by utilizing waste heat of titanium dioxide calcinator |
| CN105439105B (en) | 2015-12-22 | 2017-10-10 | 江苏久吾高科技股份有限公司 | The integrated processing recovery process of spent acid film and device in a kind of production process of titanium pigment |
| CN108840373A (en) * | 2018-09-05 | 2018-11-20 | 襄阳龙蟒钛业有限公司 | A kind of method that titanium pigment waste acid recycles |
| CN111517397A (en) | 2020-06-01 | 2020-08-11 | 江苏泰特联合环保科技有限公司 | A three-stage negative pressure evaporation crystallization treatment process and device for titanium dioxide waste sulfuric acid |
| CN112978805A (en) * | 2021-01-26 | 2021-06-18 | 北京科技大学 | Comprehensive recovery method of titanium, iron and sulfate radicals in titanium white waste acid |
-
2022
- 2022-12-14 CN CN202211598908.8A patent/CN116002768A/en active Pending
-
2023
- 2023-12-12 ZA ZA2023/11407A patent/ZA202311407B/en unknown
- 2023-12-14 EP EP23216801.3A patent/EP4389707B1/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| ZA202311407B (en) | 2024-06-26 |
| EP4389707C0 (en) | 2025-05-28 |
| EP4389707A1 (en) | 2024-06-26 |
| CN116002768A (en) | 2023-04-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4389707A1 (en) | Method for recycling ferrous sulfate heptahydrate and sulfuric acid from waste acid in titanium dioxide production | |
| CN108164075B (en) | Recycling treatment system and method for cobaltic-cobaltous wastewater | |
| CN110627095A (en) | A method of extracting lithium from alumina production process and preparing battery-grade lithium carbonate | |
| CN100581994C (en) | Concentrating and impurity removing method for dilute sulfuric acid in titanium dioxide powder production process by employing sulfuric acid process | |
| CN113073202B (en) | A method for comprehensive treatment of liquid after vanadium slag extraction of vanadium acid ammonium salt and vanadium precipitation | |
| CN110510648B (en) | Method for separating and recovering aluminum, potassium and ammonium from mixed solution containing aluminum sulfate, potassium sulfate and ammonium sulfate | |
| CN101538023A (en) | Processing method for titanium pigment waste acid | |
| CN116024440B (en) | A method for extracting lithium from sodium sulfate subtype salt lake brine by adsorption-extraction | |
| CN115893456B (en) | A method for flash evaporation and crystallization of concentrated sodium potassium sulfate solution for extracting lithium from lepidolite | |
| CN115286019A (en) | Method for producing high-purity lithium carbonate from spodumene | |
| CN111945016A (en) | Method for selectively extracting lithium from anode and cathode powder of waste lithium ion battery by roasting method | |
| CN115745238A (en) | Titanium white waste acid two-step freezing crystallization coupling integrated membrane zero discharge treatment method | |
| WO2023036048A1 (en) | Method and system for recycling sintered ash | |
| CN116654959B (en) | A method for producing battery-grade lithium carbonate via gas-liquid cycle | |
| CN117509688A (en) | An efficient full-component recycling method for waste lithium iron phosphate cathode materials | |
| GB2637410A (en) | Energy-saving treatment system and process for salt-containing and heavy metal-containing ammonia-nitrogen wastewater | |
| CN115818603A (en) | Method for preparing battery-grade iron phosphate from residues generated after lithium extraction by oxidizing lithium iron phosphate positive electrode powder containing copper, aluminum and graphite | |
| CN105753241A (en) | Method for reduction, evaporation and concentration treatment of wastewater produced by acidic precipitation of vanadate-leaching solution | |
| CN110697739A (en) | A method for preparing anhydrous lithium chloride by leaching lithium in aluminum-based lithium-rich slag | |
| CN115924940A (en) | Method for extracting lithium from sodium sulfate subtype alkaline salt lake | |
| CN101049915A (en) | Method for comprehensive using tail gas of rotary kiln and dilute sulfuric acid in procedure of producing white titanium pigment through sulfuric acid method | |
| CN118929709A (en) | A method for treating lithium carbonate mother liquor by membrane concentration | |
| CN102659167B (en) | Method for preparing copper sulfate from copper-containing material without evaporating | |
| CN118405711A (en) | Method for recovering lithium sodium potassium rubidium aluminum from lepidolite lithium extraction slag | |
| CN116332208A (en) | A method for preparing battery-grade lithium hydroxide monohydrate from spodumene acid leaching solution |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20231214 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20250109 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Ref country code: DE Ref legal event code: R096 Ref document number: 602023003711 Country of ref document: DE |
|
| U01 | Request for unitary effect filed |
Effective date: 20250617 |
|
| U07 | Unitary effect registered |
Designated state(s): AT BE BG DE DK EE FI FR IT LT LU LV MT NL PT RO SE SI Effective date: 20250701 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250828 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250829 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250828 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250928 |
|
| U20 | Renewal fee for the european patent with unitary effect paid |
Year of fee payment: 3 Effective date: 20251110 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250528 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260409 |
|
| 26N | No opposition filed |
Effective date: 20260303 |