EP4137289A1 - Core and method for molding structure - Google Patents
Core and method for molding structure Download PDFInfo
- Publication number
- EP4137289A1 EP4137289A1 EP21787678.8A EP21787678A EP4137289A1 EP 4137289 A1 EP4137289 A1 EP 4137289A1 EP 21787678 A EP21787678 A EP 21787678A EP 4137289 A1 EP4137289 A1 EP 4137289A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- skin
- die
- stringer
- core
- structural body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C70/00—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts
- B29C70/04—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts comprising reinforcements only, e.g. self-reinforcing plastics
- B29C70/28—Shaping operations therefor
- B29C70/30—Shaping by lay-up, i.e. applying fibres, tape or broadsheet on a mould, former or core; Shaping by spray-up, i.e. spraying of fibres on a mould, former or core
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29D—PRODUCING PARTICULAR ARTICLES FROM PLASTICS OR FROM SUBSTANCES IN A PLASTIC STATE
- B29D99/00—Subject matter not provided for in other groups of this subclass
- B29D99/001—Producing wall or panel-like structures, e.g. for hulls, fuselages, or buildings
- B29D99/0014—Producing wall or panel-like structures, e.g. for hulls, fuselages, or buildings provided with ridges or ribs, e.g. joined ribs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C33/00—Moulds or cores; Details thereof or accessories therefor
- B29C33/38—Moulds or cores; Details thereof or accessories therefor characterised by the material or the manufacturing process
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C33/00—Moulds or cores; Details thereof or accessories therefor
- B29C33/76—Cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C70/00—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts
- B29C70/04—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts comprising reinforcements only, e.g. self-reinforcing plastics
- B29C70/28—Shaping operations therefor
- B29C70/40—Shaping or impregnating by compression not applied
- B29C70/42—Shaping or impregnating by compression not applied for producing articles of definite length, i.e. discrete articles
- B29C70/44—Shaping or impregnating by compression not applied for producing articles of definite length, i.e. discrete articles using isostatic pressure, e.g. pressure difference-moulding, vacuum bag-moulding, autoclave-moulding or expanding rubber-moulding
- B29C70/446—Moulding structures having an axis of symmetry or at least one channel, e.g. tubular structures, frames
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C70/00—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts
- B29C70/04—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts comprising reinforcements only, e.g. self-reinforcing plastics
- B29C70/28—Shaping operations therefor
- B29C70/40—Shaping or impregnating by compression not applied
- B29C70/42—Shaping or impregnating by compression not applied for producing articles of definite length, i.e. discrete articles
- B29C70/46—Shaping or impregnating by compression not applied for producing articles of definite length, i.e. discrete articles using matched moulds, e.g. for deforming sheet moulding compounds [SMC] or prepregs
- B29C70/462—Moulding structures having an axis of symmetry or at least one channel, e.g. tubular structures, frames
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C70/00—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts
- B29C70/04—Shaping composites, i.e. plastics material comprising reinforcements, fillers or preformed parts, e.g. inserts comprising reinforcements only, e.g. self-reinforcing plastics
- B29C70/28—Shaping operations therefor
- B29C70/54—Component parts, details or accessories; Auxiliary operations, e.g. feeding or storage of prepregs or SMC after impregnation or during ageing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C33/00—Moulds or cores; Details thereof or accessories therefor
- B29C33/44—Moulds or cores; Details thereof or accessories therefor with means for, or specially constructed to facilitate, the removal of articles, e.g. of undercut articles
- B29C33/48—Moulds or cores; Details thereof or accessories therefor with means for, or specially constructed to facilitate, the removal of articles, e.g. of undercut articles with means for collapsing or disassembling
- B29C33/485—Moulds or cores; Details thereof or accessories therefor with means for, or specially constructed to facilitate, the removal of articles, e.g. of undercut articles with means for collapsing or disassembling cores or mandrels
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2105/00—Condition, form or state of moulded material or of the material to be shaped
- B29K2105/06—Condition, form or state of moulded material or of the material to be shaped containing reinforcements, fillers or inserts
- B29K2105/08—Condition, form or state of moulded material or of the material to be shaped containing reinforcements, fillers or inserts of continuous length, e.g. cords, rovings, mats, fabrics, strands or yarns
- B29K2105/0872—Prepregs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2305/00—Use of metals, their alloys or their compounds, as reinforcement
- B29K2305/08—Transition metals
- B29K2305/12—Iron
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2307/00—Use of elements other than metals as reinforcement
- B29K2307/04—Carbon
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29L—INDEXING SCHEME ASSOCIATED WITH SUBCLASS B29C, RELATING TO PARTICULAR ARTICLES
- B29L2031/00—Other particular articles
- B29L2031/30—Vehicles, e.g. ships or aircraft, or body parts thereof
- B29L2031/3076—Aircrafts
- B29L2031/3082—Fuselages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2260/00—Layered product comprising an impregnated, embedded, or bonded layer wherein the layer comprises an impregnation, embedding, or binder material
- B32B2260/02—Composition of the impregnated, bonded or embedded layer
- B32B2260/021—Fibrous or filamentary layer
- B32B2260/023—Two or more layers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2260/00—Layered product comprising an impregnated, embedded, or bonded layer wherein the layer comprises an impregnation, embedding, or binder material
- B32B2260/04—Impregnation, embedding, or binder material
- B32B2260/046—Synthetic resin
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2262/00—Composition or structural features of fibres which form a fibrous or filamentary layer or are present as additives
- B32B2262/10—Inorganic fibres
- B32B2262/106—Carbon fibres, e.g. graphite fibres
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B5/00—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts
- B32B5/02—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by structural features of a fibrous or filamentary layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B5/00—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts
- B32B5/22—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by the presence of two or more layers which are next to each other and are fibrous, filamentary, formed of particles or foamed
- B32B5/24—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by the presence of two or more layers which are next to each other and are fibrous, filamentary, formed of particles or foamed one layer being a fibrous or filamentary layer
- B32B5/26—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by the presence of two or more layers which are next to each other and are fibrous, filamentary, formed of particles or foamed one layer being a fibrous or filamentary layer another layer next to it also being fibrous or filamentary
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02T—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO TRANSPORTATION
- Y02T50/00—Aeronautics or air transport
- Y02T50/40—Weight reduction
Definitions
- the present disclosure relates to a core used in a step of forming a structural body including fiber-reinforced resin and a method of forming the structural body by using the core.
- a structural body formed by integrally molding a skin made of fiber-reinforced resin and a beam-shaped stringer has been devised.
- a stringer having a hat-shaped section that is open toward the skin can be used.
- the stringer having the hat-shaped section is advantageous in that this stringer easily follows a change in the section of the structural body and has high strength for its weight.
- a core needs to be inserted in a space between the skin and the stringer (see PTL 1, for example).
- a surface of the core which supports the skin i.e., a surface of the core which contacts the skin be not partially deformed.
- the core made of a hard material is low in flexibility, and therefore, it is not easy to pull out the core after the forming.
- the present disclosure was made under these circumstances, and an object of the present disclosure is to provide a core that is easily pulled out after forming and includes a surface which contacts a skin and is hardly partially deformed, and also provide a method of forming a structural body.
- a core according to one aspect of the present disclosure is a core that is inserted into a space between a skin and a stringer in a step of integrally molding the skin and the stringer, the skin including fiber-reinforced resin, the stringer having a hat-shaped section that is open toward the skin.
- the core includes: a first die that extends along a longitudinal direction of the stringer and contacts the skin; and a second die that extends along the longitudinal direction of the stringer, is located at an opposite side of the skin across the first die, and is larger in thickness than the first die.
- the second die includes a material that is softer than the first die.
- the second die includes a slit perpendicular to the longitudinal direction of the stringer.
- the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed.
- the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- a method of forming a structural body according to one aspect of the present disclosure includes: inserting the core into the space between the skin and the stringer; in this state, integrally molding the skin and the stringer; and then, pulling out the core from the space.
- the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed.
- the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- the present disclosure can provide a core that is easily pulled out after forming and includes a surface which contacts a skin and is hardly partially deformed, and also provide a method of forming a structural body.
- FIG. 1 is a front view of the structural body 101 and shows a part of the structural body 101.
- the structural body 101 is an airframe of an aircraft.
- the structural body 101 includes a skin 102 and stringers 103.
- FIG. 1 shows one of the stringers 103.
- the shape of the structural body 101 is not limited and may be a flat plate shape or a cylindrical shape.
- the skin 102 is a portion corresponding to a surface of the structural body 101.
- the thickness of the skin 102 is not constant.
- the skin 102 is formed in such a manner that: sheet-shaped prepregs are prepared by impregnating fibers, such as carbon, with resin; and the prepregs are laminated on each other and are cured.
- the skin 102 is made of fiber-reinforced resin.
- the thickness of the skin 102 can be adjusted by the number of prepregs laminated.
- the resin of the skin 102 of the present embodiment is thermoplastic resin but may be thermosetting resin.
- the stringer 103 is a portion which is located inside the skin 102 and formed integrally with the skin 102.
- the stringer 103 serves as a beam and extends in a predetermined direction (direction perpendicular to a paper surface of FIG. 1 ).
- the stringer 103 extends along an axial direction of the structural body 101.
- the stringer 103 of the present embodiment is made of the same material (i.e., the fiber-reinforced resin) as the skin 102.
- the stringer 103 may be made of a different material from the skin 102.
- the stringer 103 may be made of an invar alloy.
- a direction in which the stringer 103 extends is referred to as a "longitudinal direction,” and a section perpendicular to the longitudinal direction is simply referred to as a “section.”
- a direction in which the skin 102 extends in a sectional view is referred to as a "width direction,” and a direction along a perpendicular line of the skin 102 in the sectional view is referred to as a “perpendicular direction.” In some cases, the perpendicular direction does not coincide with a vertical direction.
- the stringer 103 has a hat-shaped section that is open toward the skin 102.
- the stringer 103 includes a bottom surface portion 104, two side surface portions 105, and two flange portions 106.
- the bottom surface portion 104 is located farthest from the skin 102.
- the two side surface portions 105 extend from both width direction ends of the bottom surface portion 104 toward the skin 102.
- the two flange portions 106 extend from the respective side surface portions 105 outward in the width direction while contacting the skin 102.
- the two side surface portions 105 are inclined relative to the perpendicular direction so as to extend away from each other in the width direction.
- a space 107 is between the skin 102 and the stringer 103.
- the space 107 extends in the longitudinal direction and has a trapezoidal shape in the sectional view.
- the core 100 is inserted into the space 107.
- FIGS. 2A to 2G are diagrams showing the step of forming the structural body 101.
- the below-described step of forming the structural body 101 is one example in which the skin 102 is made of thermoplastic resin.
- the skin 102 is made of thermosetting resin, a different step is performed.
- the stringer 103 is placed in a groove 109 of a base die 108 prepared in advance.
- the base die 108 has a shape corresponding to the shape of the completed structural body 101.
- the base die 108 has a plate shape or a semi-circular section.
- the core 100 is inserted into the stringer 103. Details of the core 100 will be described later.
- the skin 102 is formed along the surface of the base die 108 and the surface of the core 100. As described above, the skin 102 is formed by laminating the prepregs. At this time, the skin 102 is not yet cured and is not yet joined to the stringer 103.
- heat is applied to the skin 102, and force is applied to the surface of the skin 102 with a pressurizer 110. At this time, the force is partially applied to the skin 102. Moreover, the temperature of the skin 102 becomes a high temperature, such as 350°C. As above, when the skin 102 is pressurized while being heated, the skin 102 is cured and joined to the stringer 103. To be specific, the skin 102 and the stringer 103 are integrally molded.
- the core 100 is pulled out from the space 107 between the skin 102 and the stringer 103.
- the structural body 101 in which the skin 102 and the stringer 103 are integrated with each other is taken out from the base die 108. This is the step of forming the structural body 101.
- FIG. 3 is a front view of the skin 102 and the core 100.
- FIG. 4 is a sectional view taken along line IV-IV of FIG. 3.
- FIGS. 3 and 4 show that the core 100 is in the space 107 between the skin 102 and the stringer 103. The same is true in FIG. 5 described later.
- the thickness of the skin 102 of the present embodiment is not constant and varies depending on the position in the longitudinal direction. As a result, the space 107 between the skin 102 and the stringer 103 is displaced as it extends in the longitudinal direction.
- the core 100 according to the present embodiment can be utilized for the forming of the structural body 101.
- the core 100 includes a first die 10 and a second die 20 which are separable from each other.
- the first die 10 is a die that contacts the skin 102 and extends in the longitudinal direction.
- the first die 10 of the present embodiment includes plates 11 laminated on each other in the perpendicular direction.
- the number of plates 11 in the first die 10 is not especially limited but is desirably three or more. When three or more plates 11 are laminated on each other, there exists the plate 11 sandwiched between the plates 11. When the surfaces of the plates 11 are made smooth, the plate 11 between the plates 11 can be easily pulled out.
- a dimension of each plate 11 of the first die 10 in the width direction is not especially limited. However, it is desirable that to surely support the skin 102, the dimension of each plate 11 in the width direction be set such that a gap between the plate 11 and the stringer 103 (the flange portion 106 or the side surface portion 105) becomes small. When width direction end portions of the plates 11 contact the stringer 103, the plates 11 are supported by the stringer 103, and therefore, stabilized.
- the first die 10 i.e., the plates 11
- the first die 10 needs to be made of a material that can withstand the heat applied in the step of forming the structural body 101.
- the surfaces of the first die 10 be smooth such that the friction of the first die 10 with the skin 102 when the core 100 is pulled out does not become large.
- the first die 10 may include stainless steel.
- the first die 10 When the first die 10 is made of a relatively hard material, the first die 10 becomes low in flexibility, and therefore, it may not be easy to pull out the core after the forming. However, in the present embodiment, since the plates 11 of the first die 10 can be made thin, the plates 11 are high in flexibility. Therefore, the plates 11 are easily pulled out after the forming, and therefore, the core 100 is easily pulled out.
- the second die 20 is a die that is located at an opposite side of the skin 102 across the first die 10.
- the second die 20 extends in the longitudinal direction and has a rectangular section.
- the second die 20 may have a trapezoidal sectional shape corresponding to the sectional shape of the stringer 103.
- the second die 20 of the present embodiment is larger in thickness (dimension in the perpendicular direction) than the first die 10.
- An upper surface 21 of the second die 20 contacts the first die 10, and a lower surface 22 of the second die 20 contacts the bottom surface portion 104 of the stringer 103.
- a structure (not shown) may be between the second die 20 and the first die 10 or between the second die 20 and the bottom surface portion 104 of the stringer 103.
- the second die 20 of the present embodiment includes a material that is softer than the first die 10. Since the first die 10 is between the second die 20 and the skin 102, the force partially applied to the skin 102 is dispersedly transmitted to the second die 20. Thus, the force is not partially applied to the second die, and therefore, the second die does not have to have high hardness unlike the first die 10. To pull out the second die 20, high hardness is rather undesirable. Moreover, the second die 20 also needs to be made of a material that can withstand the heat applied in the step of forming the structural body 101. Based on these, the second die 20 may include fluorocarbon resin, polyimide, or aluminum.
- the second die 20 of the present embodiment includes slit 23 perpendicular to the longitudinal direction. With this, portions of the second die 20 which are adjacent to each other across the slit 23 can be displaced relative to each other. As a result, the core 100 according to the present embodiment easily follows the displacement of the space 107 between the skin 102 and the stringer 103 and is easily pulled out.
- the number of slits 23 of the second die 20 is not limited.
- the slit 23 is open on the lower surface 22 of the second die 20 and extends from the lower surface 22 toward the skin 102.
- the slit 23 may be open on the the upper surface 21 of the second die 20 and extend toward the bottom surface portion 104 of the stringer 103.
- a dimension of the slit 23 in the perpendicular direction is not limited, and may be, for example, 50% or more of a dimension of the second die 20 in the perpendicular direction.
- the core 100 in the work of pulling out the core 100 in the step of forming the structural body 101, first, the plate 11 that is most easily pulled out is pulled out, i.e., the plate 11 between the plates 11 is pulled out. Next, the plates 11 each of which is not between the plates 11 is pulled out. Finally, the second die 20 is pulled out. Since these structures easily follow the displacement of the space 107 between the skin 102 and the stringer 103, the structures can be easily pulled out.
- the core according to the embodiment is a core that is inserted into a space between a skin and a stringer in a step of integrally molding the skin and the stringer, the skin including fiber-reinforced resin, the stringer having a hat-shaped section that is open toward the skin.
- the core includes: a first die that extends along a longitudinal direction of the stringer and contacts the skin; and a second die that extends along the longitudinal direction of the stringer and is located at an opposite side of the skin across the first die.
- the second die includes a material that is softer than the first die.
- the second die includes a slit perpendicular to the longitudinal direction of the stringer.
- the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed.
- the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- the first die includes plates laminated on each other in a direction along a perpendicular line of the skin.
- the first die includes the plates. Therefore, the first die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- a thickness of the second die in a direction along a perpendicular line of the skin is larger than a thickness of the first die in the direction along the perpendicular line of the skin.
- a ratio of the second die, which is made of a relatively soft material and includes the slit, to the entire core is large. Therefore, the core is further easily pulled out after the forming.
- the first die includes stainless steel
- the second die includes fluorocarbon resin, polyimide, or aluminum.
- the core can withstand the heat applied in the step of integral molding and can reduce the friction generated when being pulled out.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Composite Materials (AREA)
- Architecture (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Moulding By Coating Moulds (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
Abstract
Description
- The present disclosure relates to a core used in a step of forming a structural body including fiber-reinforced resin and a method of forming the structural body by using the core.
- A structural body formed by integrally molding a skin made of fiber-reinforced resin and a beam-shaped stringer has been devised. As the stringer, a stringer having a hat-shaped section that is open toward the skin can be used. The stringer having the hat-shaped section is advantageous in that this stringer easily follows a change in the section of the structural body and has high strength for its weight. However, in the step of integrally molding the skin and the stringer having the hat-shaped section, a core needs to be inserted in a space between the skin and the stringer (see PTL 1, for example).
- PTL 1:
Japanese Laid-Open Patent Application Publication No. 2015-142993 - In the step of integrally molding the skin and the stringer, large force may be partially applied to an outer surface of the skin. Therefore, it is desirable that a surface of the core which supports the skin, i.e., a surface of the core which contacts the skin be not partially deformed. However, the core made of a hard material is low in flexibility, and therefore, it is not easy to pull out the core after the forming.
- The present disclosure was made under these circumstances, and an object of the present disclosure is to provide a core that is easily pulled out after forming and includes a surface which contacts a skin and is hardly partially deformed, and also provide a method of forming a structural body.
- A core according to one aspect of the present disclosure is a core that is inserted into a space between a skin and a stringer in a step of integrally molding the skin and the stringer, the skin including fiber-reinforced resin, the stringer having a hat-shaped section that is open toward the skin. The core includes: a first die that extends along a longitudinal direction of the stringer and contacts the skin; and a second die that extends along the longitudinal direction of the stringer, is located at an opposite side of the skin across the first die, and is larger in thickness than the first die. The second die includes a material that is softer than the first die. The second die includes a slit perpendicular to the longitudinal direction of the stringer.
- According to this configuration, the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed. Moreover, the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- A method of forming a structural body according to one aspect of the present disclosure includes: inserting the core into the space between the skin and the stringer; in this state, integrally molding the skin and the stringer; and then, pulling out the core from the space.
- According to this forming method, the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed. Moreover, the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- According to the above configuration, the present disclosure can provide a core that is easily pulled out after forming and includes a surface which contacts a skin and is hardly partially deformed, and also provide a method of forming a structural body.
-
-
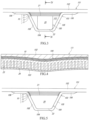
FIG. 1 is a front view of a structural body formed by using a core. -
FIGS. 2A to 2G are diagrams showing a step of forming the structural body. -
FIG. 3 is a front view of the core. -
FIG. 4 is a sectional view taken along line IV-IV ofFIG. 3 . -
FIG. 5 is a front view of the core according to Modified Example. - Hereinafter, a
core 100 according to the present embodiment will be described. First, astructural body 101 formed by using thecore 100 will be described.FIG. 1 is a front view of thestructural body 101 and shows a part of thestructural body 101. As one example, thestructural body 101 is an airframe of an aircraft. Thestructural body 101 includes askin 102 andstringers 103.FIG. 1 shows one of thestringers 103. The shape of thestructural body 101 is not limited and may be a flat plate shape or a cylindrical shape. - The
skin 102 is a portion corresponding to a surface of thestructural body 101. In the present embodiment, the thickness of theskin 102 is not constant. Theskin 102 is formed in such a manner that: sheet-shaped prepregs are prepared by impregnating fibers, such as carbon, with resin; and the prepregs are laminated on each other and are cured. To be specific, theskin 102 is made of fiber-reinforced resin. The thickness of theskin 102 can be adjusted by the number of prepregs laminated. The resin of theskin 102 of the present embodiment is thermoplastic resin but may be thermosetting resin. - The
stringer 103 is a portion which is located inside theskin 102 and formed integrally with theskin 102. Thestringer 103 serves as a beam and extends in a predetermined direction (direction perpendicular to a paper surface ofFIG. 1 ). When thestructural body 101 has a tubular shape, thestringer 103 extends along an axial direction of thestructural body 101. Thestringer 103 of the present embodiment is made of the same material (i.e., the fiber-reinforced resin) as theskin 102. However, thestringer 103 may be made of a different material from theskin 102. For example, thestringer 103 may be made of an invar alloy. - Hereinafter, a direction in which the
stringer 103 extends is referred to as a "longitudinal direction," and a section perpendicular to the longitudinal direction is simply referred to as a "section." A direction in which theskin 102 extends in a sectional view is referred to as a "width direction," and a direction along a perpendicular line of theskin 102 in the sectional view is referred to as a "perpendicular direction." In some cases, the perpendicular direction does not coincide with a vertical direction. - The
stringer 103 has a hat-shaped section that is open toward theskin 102. Specifically, thestringer 103 includes abottom surface portion 104, twoside surface portions 105, and twoflange portions 106. Thebottom surface portion 104 is located farthest from theskin 102. The twoside surface portions 105 extend from both width direction ends of thebottom surface portion 104 toward theskin 102. The twoflange portions 106 extend from the respectiveside surface portions 105 outward in the width direction while contacting theskin 102. The twoside surface portions 105 are inclined relative to the perpendicular direction so as to extend away from each other in the width direction. - Since the
skin 102 and thestringer 103 are as above, aspace 107 is between theskin 102 and thestringer 103. Thespace 107 extends in the longitudinal direction and has a trapezoidal shape in the sectional view. In a step of integrally molding theskin 102 and thestringer 103, thecore 100 is inserted into thespace 107. - Next, a step of forming the above
structural body 101, i.e., the step of integrally molding theskin 102 and thestringer 103 will be described.FIGS. 2A to 2G are diagrams showing the step of forming thestructural body 101. The below-described step of forming thestructural body 101 is one example in which theskin 102 is made of thermoplastic resin. For example, when theskin 102 is made of thermosetting resin, a different step is performed. - In the forming step of the present embodiment, first, as shown in
FIGS. 2A and 2B , thestringer 103 is placed in agroove 109 of a base die 108 prepared in advance. The base die 108 has a shape corresponding to the shape of the completedstructural body 101. For example, the base die 108 has a plate shape or a semi-circular section. Next, as shown inFIG. 2C , thecore 100 is inserted into thestringer 103. Details of thecore 100 will be described later. - Next, as shown in
FIG. 2D , theskin 102 is formed along the surface of the base die 108 and the surface of thecore 100. As described above, theskin 102 is formed by laminating the prepregs. At this time, theskin 102 is not yet cured and is not yet joined to thestringer 103. - Next, as shown in
FIG. 2E , heat is applied to theskin 102, and force is applied to the surface of theskin 102 with apressurizer 110. At this time, the force is partially applied to theskin 102. Moreover, the temperature of theskin 102 becomes a high temperature, such as 350°C. As above, when theskin 102 is pressurized while being heated, theskin 102 is cured and joined to thestringer 103. To be specific, theskin 102 and thestringer 103 are integrally molded. - Next, as shown in
FIG. 2F , thecore 100 is pulled out from thespace 107 between theskin 102 and thestringer 103. Finally, as shown inFIG. 2G , thestructural body 101 in which theskin 102 and thestringer 103 are integrated with each other is taken out from the base die 108. This is the step of forming thestructural body 101. - Next, the
core 100 according to the present embodiment will be described.FIG. 3 is a front view of theskin 102 and thecore 100.FIG. 4 is a sectional view taken along line IV-IV ofFIG. 3. FIGS. 3 and 4 show that thecore 100 is in thespace 107 between theskin 102 and thestringer 103. The same is true inFIG. 5 described later. - As described above, the thickness of the
skin 102 of the present embodiment is not constant and varies depending on the position in the longitudinal direction. As a result, thespace 107 between theskin 102 and thestringer 103 is displaced as it extends in the longitudinal direction. Thecore 100 according to the present embodiment can be utilized for the forming of thestructural body 101. - As shown in
FIG. 3 , thecore 100 according to the present embodiment includes afirst die 10 and asecond die 20 which are separable from each other. - The
first die 10 is a die that contacts theskin 102 and extends in the longitudinal direction. The first die 10 of the present embodiment includesplates 11 laminated on each other in the perpendicular direction. The number ofplates 11 in thefirst die 10 is not especially limited but is desirably three or more. When three ormore plates 11 are laminated on each other, there exists theplate 11 sandwiched between theplates 11. When the surfaces of theplates 11 are made smooth, theplate 11 between theplates 11 can be easily pulled out. - Moreover, a dimension of each
plate 11 of thefirst die 10 in the width direction is not especially limited. However, it is desirable that to surely support theskin 102, the dimension of eachplate 11 in the width direction be set such that a gap between theplate 11 and the stringer 103 (theflange portion 106 or the side surface portion 105) becomes small. When width direction end portions of theplates 11 contact thestringer 103, theplates 11 are supported by thestringer 103, and therefore, stabilized. - In the step of forming the
structural body 101, force is partially applied to the skin 102 (seeFIG. 2E ). Therefore, it is desirable that the first die 10 (i.e., the plates 11) be made of a relatively hard material so as not to be partially deformed. Moreover, thefirst die 10 needs to be made of a material that can withstand the heat applied in the step of forming thestructural body 101. Furthermore, it is desirable that the surfaces of thefirst die 10 be smooth such that the friction of thefirst die 10 with theskin 102 when thecore 100 is pulled out does not become large. Based on these, thefirst die 10 may include stainless steel. - When the
first die 10 is made of a relatively hard material, thefirst die 10 becomes low in flexibility, and therefore, it may not be easy to pull out the core after the forming. However, in the present embodiment, since theplates 11 of thefirst die 10 can be made thin, theplates 11 are high in flexibility. Therefore, theplates 11 are easily pulled out after the forming, and therefore, thecore 100 is easily pulled out. - The
second die 20 is a die that is located at an opposite side of theskin 102 across thefirst die 10. Thesecond die 20 extends in the longitudinal direction and has a rectangular section. However, as shown inFIG. 5 , thesecond die 20 may have a trapezoidal sectional shape corresponding to the sectional shape of thestringer 103. Moreover, thesecond die 20 of the present embodiment is larger in thickness (dimension in the perpendicular direction) than thefirst die 10. - An
upper surface 21 of the second die 20 contacts thefirst die 10, and alower surface 22 of the second die 20 contacts thebottom surface portion 104 of thestringer 103. A structure (not shown) may be between thesecond die 20 and thefirst die 10 or between thesecond die 20 and thebottom surface portion 104 of thestringer 103. - The second die 20 of the present embodiment includes a material that is softer than the
first die 10. Since thefirst die 10 is between thesecond die 20 and theskin 102, the force partially applied to theskin 102 is dispersedly transmitted to thesecond die 20. Thus, the force is not partially applied to the second die, and therefore, the second die does not have to have high hardness unlike thefirst die 10. To pull out thesecond die 20, high hardness is rather undesirable. Moreover, thesecond die 20 also needs to be made of a material that can withstand the heat applied in the step of forming thestructural body 101. Based on these, thesecond die 20 may include fluorocarbon resin, polyimide, or aluminum. - Moreover, the
second die 20 of the present embodiment includes slit 23 perpendicular to the longitudinal direction. With this, portions of thesecond die 20 which are adjacent to each other across theslit 23 can be displaced relative to each other. As a result, thecore 100 according to the present embodiment easily follows the displacement of thespace 107 between theskin 102 and thestringer 103 and is easily pulled out. The number ofslits 23 of thesecond die 20 is not limited. - In the present embodiment, the
slit 23 is open on thelower surface 22 of thesecond die 20 and extends from thelower surface 22 toward theskin 102. However, theslit 23 may be open on the theupper surface 21 of thesecond die 20 and extend toward thebottom surface portion 104 of thestringer 103. Furthermore, a dimension of theslit 23 in the perpendicular direction is not limited, and may be, for example, 50% or more of a dimension of thesecond die 20 in the perpendicular direction. - The foregoing has described the core 100 according to the present embodiment. In the present embodiment, in the work of pulling out the
core 100 in the step of forming thestructural body 101, first, theplate 11 that is most easily pulled out is pulled out, i.e., theplate 11 between theplates 11 is pulled out. Next, theplates 11 each of which is not between theplates 11 is pulled out. Finally, thesecond die 20 is pulled out. Since these structures easily follow the displacement of thespace 107 between theskin 102 and thestringer 103, the structures can be easily pulled out. - As above, the core according to the embodiment is a core that is inserted into a space between a skin and a stringer in a step of integrally molding the skin and the stringer, the skin including fiber-reinforced resin, the stringer having a hat-shaped section that is open toward the skin. The core includes: a first die that extends along a longitudinal direction of the stringer and contacts the skin; and a second die that extends along the longitudinal direction of the stringer and is located at an opposite side of the skin across the first die. The second die includes a material that is softer than the first die. The second die includes a slit perpendicular to the longitudinal direction of the stringer.
- According to this configuration, the first die that contacts the skin is made of a relatively hard material. Therefore, a surface of the first die which contacts the skin can be prevented from being partially deformed. Moreover, the second die located at an opposite side of the skin is made of a relatively soft material and includes the slit. Therefore, the second die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- Moreover, in the core according to the embodiment, the first die includes plates laminated on each other in a direction along a perpendicular line of the skin.
- According to this configuration, the first die includes the plates. Therefore, the first die easily follows the displacement of the space between the skin and the stringer. As a result, the core is easily pulled out after the forming.
- Moreover, in the core according to the embodiment, a thickness of the second die in a direction along a perpendicular line of the skin is larger than a thickness of the first die in the direction along the perpendicular line of the skin.
- According to this configuration, a ratio of the second die, which is made of a relatively soft material and includes the slit, to the entire core is large. Therefore, the core is further easily pulled out after the forming.
- Moreover, in the core according to the embodiment, the first die includes stainless steel, and the second die includes fluorocarbon resin, polyimide, or aluminum.
- According to this configuration, the core can withstand the heat applied in the step of integral molding and can reduce the friction generated when being pulled out.
-
- 10
- first die
- 11
- plate
- 20
- second die
- 23
- slit
- 100
- core
- 101
- structural body
- 102
- skin
- 103
- stringer
- 107
- space
Claims (5)
- A core that is inserted into a space between a skin and a stringer in a step of integrally molding the skin and the stringer, the skin including fiber-reinforced resin, the stringer having a hat-shaped section that is open toward the skin,
the core comprising:a first die that extends along a longitudinal direction of the stringer and contacts the skin; anda second die that extends along the longitudinal direction of the stringer and is located at an opposite side of the skin across the first die, wherein:the second die includes a material that is softer than the first die; andthe second die includes a slit perpendicular to the longitudinal direction of the stringer. - The core according to claim 1, wherein the first die includes plates laminated on each other in a direction along a perpendicular line of the skin.
- The core according to claim 1 or 2, wherein a thickness of the second die in a direction along a perpendicular line of the skin is larger than a thickness of the first die in the direction along the perpendicular line of the skin.
- The core according to any one of claims 1 to 3, wherein:the first die includes stainless steel; andthe second die includes fluorocarbon resin, polyimide, or aluminum.
- A method of forming a structural body,
the method comprising:inserting the core according to any one of claims 1 to 4 into the space between the skin and the stringer;in this state, integrally molding the skin and the stringer; andthen, pulling out the core from the space.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US202063009149P | 2020-04-13 | 2020-04-13 | |
| PCT/JP2021/015317 WO2021210580A1 (en) | 2020-04-13 | 2021-04-13 | Core and method for molding structure |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4137289A1 true EP4137289A1 (en) | 2023-02-22 |
| EP4137289A4 EP4137289A4 (en) | 2024-04-24 |
Family
ID=78084859
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP21787678.8A Withdrawn EP4137289A4 (en) | 2020-04-13 | 2021-04-13 | CORE AND METHOD FOR FORMING A STRUCTURE |
| EP21788852.8A Active EP4137290B1 (en) | 2020-04-13 | 2021-04-13 | Core and method for molding structure |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP21788852.8A Active EP4137290B1 (en) | 2020-04-13 | 2021-04-13 | Core and method for molding structure |
Country Status (4)
| Country | Link |
|---|---|
| US (3) | US20230131937A1 (en) |
| EP (2) | EP4137289A4 (en) |
| JP (2) | JP7261356B2 (en) |
| WO (2) | WO2021210579A1 (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR3159546B1 (en) * | 2024-02-28 | 2026-01-09 | Loiretech Ingenierie | Core for molding a hollow composite profile and molding method using such a core |
Family Cites Families (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US875097A (en) * | 1906-08-16 | 1907-12-31 | George F Mckee | Collapsible core. |
| US1371525A (en) * | 1920-06-11 | 1921-03-15 | Charles F Strausbaugh | Mold-core |
| US1394558A (en) * | 1920-12-29 | 1921-10-25 | Rub Tex Products Inc | Process and apparatus for the manufacture of rubber jars |
| US2445290A (en) * | 1940-12-24 | 1948-07-13 | Holoplast Ltd | Hollow cavitied bodies such as rigid hollow panel structures and method of making the same |
| US2442516A (en) * | 1946-02-04 | 1948-06-01 | William C Shriver | Compression mold |
| US2682294A (en) * | 1952-10-21 | 1954-06-29 | Langer Nicholas | Heat sealing machine of the thermal impulse type and sealing bar therefor |
| US2818618A (en) * | 1955-09-07 | 1958-01-07 | Bohn Aluminium & Brass Corp | Four-part core pin |
| US5387098A (en) * | 1992-04-23 | 1995-02-07 | The Boeing Company | Flexible reusable mandrels |
| US7293737B2 (en) * | 2004-04-20 | 2007-11-13 | The Boeing Company | Co-cured stringers and associated mandrel and fabrication method |
| US8557165B2 (en) * | 2008-10-25 | 2013-10-15 | The Boeing Company | Forming highly contoured composite parts |
| US8778117B2 (en) | 2008-12-11 | 2014-07-15 | Airbus Operations Gmbh | Method for producing an integral, reinforced fibre composite component as well as a hollow fibre composite component |
| DE102009002697B4 (en) * | 2009-04-28 | 2014-02-27 | Airbus Operations Gmbh | Mold core and method for producing a fiber composite component for the aerospace industry |
| DE102012000564B4 (en) * | 2012-01-16 | 2015-02-19 | Airbus Operations Gmbh | Forming tool and method for the manufacture of an aerodynamically shaped aircraft component made of fiber-reinforced plastic |
| DE102013222106A1 (en) * | 2013-10-30 | 2015-05-13 | Airbus Operations Gmbh | Curing tool for shell components and method for curing shell components |
| JP6209095B2 (en) | 2014-01-31 | 2017-10-04 | 三菱重工業株式会社 | FRP forming jig and FRP structure forming method |
| US9724848B2 (en) * | 2014-07-03 | 2017-08-08 | The Boeing Company | Collapsible, coiled mandrel |
| EP3205491B1 (en) * | 2016-02-09 | 2020-07-08 | Airbus Defence and Space SA | Method for manufacturing a stiffened panel made from composite material |
| US10906210B2 (en) * | 2017-01-25 | 2021-02-02 | The Boeing Company | Mandrel for composite part fabrication and repair |
| US10926435B2 (en) * | 2017-05-03 | 2021-02-23 | The Boeing Company | Foam mandrel assembly |
| US11014644B2 (en) * | 2017-10-25 | 2021-05-25 | The Boeing Company | Stiffened-cavity for modular wrap ply assembly for hat stringer |
-
2021
- 2021-04-13 WO PCT/JP2021/015316 patent/WO2021210579A1/en not_active Ceased
- 2021-04-13 WO PCT/JP2021/015317 patent/WO2021210580A1/en not_active Ceased
- 2021-04-13 EP EP21787678.8A patent/EP4137289A4/en not_active Withdrawn
- 2021-04-13 JP JP2022515396A patent/JP7261356B2/en active Active
- 2021-04-13 JP JP2022515397A patent/JP7261357B2/en active Active
- 2021-04-13 EP EP21788852.8A patent/EP4137290B1/en active Active
-
2022
- 2022-10-12 US US17/964,058 patent/US20230131937A1/en not_active Abandoned
- 2022-10-12 US US17/964,095 patent/US12214558B2/en active Active
-
2024
- 2024-03-01 US US18/592,613 patent/US20240198605A1/en active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| EP4137290B1 (en) | 2025-12-10 |
| US20230131937A1 (en) | 2023-04-27 |
| US12214558B2 (en) | 2025-02-04 |
| US20230029898A1 (en) | 2023-02-02 |
| JPWO2021210580A1 (en) | 2021-10-21 |
| WO2021210580A1 (en) | 2021-10-21 |
| EP4137290A1 (en) | 2023-02-22 |
| EP4137290A4 (en) | 2024-05-29 |
| JPWO2021210579A1 (en) | 2021-10-21 |
| WO2021210579A1 (en) | 2021-10-21 |
| JP7261356B2 (en) | 2023-04-19 |
| JP7261357B2 (en) | 2023-04-19 |
| EP4137289A4 (en) | 2024-04-24 |
| US20240198605A1 (en) | 2024-06-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1740455B1 (en) | Airfoil box and associated method | |
| US9187167B2 (en) | Method for joining two fuselage sections by creating a transverse butt joint as well as transverse butt joint connection | |
| DE102011000588A1 (en) | Superconducting magnets with improved support structure | |
| EP2301840A2 (en) | Integrated aircraft structure in composite material | |
| EP2331320B1 (en) | Fibre reinforced composite structures and method of manufacture | |
| US20230131937A1 (en) | Core and method of forming structural body | |
| EP3501972B1 (en) | A stiffener for an aircraft assembly | |
| US10259557B2 (en) | Pressure bulkhead for an aircraft fuselage, and an aircraft comprising such a pressure bulkhead | |
| EP3135926B1 (en) | Mounting structure for fixtures of an aircraft lavatory unit | |
| JP4977908B2 (en) | Anchor type clip | |
| EP3095960B1 (en) | Vane connection part structure and jet engine utilizing same | |
| US20160339668A1 (en) | Composite material structure | |
| EP3546768A1 (en) | Electromagnetic effect protective fastener with swageable termination body | |
| US12580109B2 (en) | Superconducting coil | |
| US6525536B2 (en) | Compact gradient coil assembly for MRI apparatus | |
| EP3505778B1 (en) | Structural assembly and method of assembling | |
| EP3798137A1 (en) | Pipe structure and truss structure, and artificial satellite using such structures | |
| US20150021455A1 (en) | Turbine engine support part of hybrid structure | |
| EP4079485A1 (en) | Shaping method and shaping device | |
| DE102018213128A1 (en) | Housing arrangement of an electric motor | |
| EP4678382A1 (en) | Joint member and method for manufacturing joint member | |
| US20260107393A1 (en) | Casing assembly and power supply device | |
| EP4656364A1 (en) | Composite radius fillers, assemblies including composite radius fillers, and systems and methods of forming the same | |
| JP2010025177A (en) | Fiber-reinforced plastic structure and fastening structure and manufacturing method of the same | |
| US11518495B2 (en) | Composite structural elements |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20220929 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20240326 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B29D 99/00 20100101ALI20240320BHEP Ipc: B29C 33/48 20060101ALI20240320BHEP Ipc: B29C 33/38 20060101ALI20240320BHEP Ipc: B29C 70/54 20060101ALI20240320BHEP Ipc: B29C 33/76 20060101AFI20240320BHEP |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN WITHDRAWN |
|
| 18W | Application withdrawn |
Effective date: 20240516 |