EP3514253B1 - Hot-rolled steel & method for manufacturing hot-rolled steel - Google Patents
Hot-rolled steel & method for manufacturing hot-rolled steel Download PDFInfo
- Publication number
- EP3514253B1 EP3514253B1 EP18152884.5A EP18152884A EP3514253B1 EP 3514253 B1 EP3514253 B1 EP 3514253B1 EP 18152884 A EP18152884 A EP 18152884A EP 3514253 B1 EP3514253 B1 EP 3514253B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- hot
- rolled steel
- mass
- steel
- mpa
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/58—Ferrous alloys, e.g. steel alloys containing chromium with nickel with more than 1.5% by weight of manganese
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/18—Hardening; Quenching with or without subsequent tempering
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/18—Hardening; Quenching with or without subsequent tempering
- C21D1/19—Hardening; Quenching with or without subsequent tempering by interrupted quenching
- C21D1/20—Isothermal quenching, e.g. bainitic hardening
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/18—Hardening; Quenching with or without subsequent tempering
- C21D1/25—Hardening, combined with annealing between 300 degrees Celsius and 600 degrees Celsius, i.e. heat refining ("Vergüten")
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/004—Heat treatment of ferrous alloys containing Cr and Ni
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/005—Heat treatment of ferrous alloys containing Mn
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
- C21D8/0263—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment following hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
- C21D8/0273—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0447—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the heat treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/001—Ferrous alloys, e.g. steel alloys containing N
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/42—Ferrous alloys, e.g. steel alloys containing chromium with nickel with copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/44—Ferrous alloys, e.g. steel alloys containing chromium with nickel with molybdenum or tungsten
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/48—Ferrous alloys, e.g. steel alloys containing chromium with nickel with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/50—Ferrous alloys, e.g. steel alloys containing chromium with nickel with titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/54—Ferrous alloys, e.g. steel alloys containing chromium with nickel with boron
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/001—Austenite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/002—Bainite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/008—Martensite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
Definitions
- the present invention concerns high strength hot-rolled steel and a method for manufacturing such hot-rolled steel.
- Martensitic flat steel products have for many years been manufactured using a method comprising the steps of heating a steel slab to an austenitizing temperature, hot-rolling, re-heating, quenching and tempering, or alternatively, heating a steel slab to an austenitizing temperature, hot-rolling, direct quenching and tempering.
- European patent no. EP 2,576,848 discloses a method for producing a hot-rolled steel from a steel, whose composition as percentages by weight is C 0.075 - 0.12%, Si 0.1 - 0.8%, Mn 0.8 - 1.7%, Al 0.015 - 0.08%, P less than 0.012%, S less than 0.005%, Cr 0.2 - 1.3%, Mo 0.15 - 0.80%, Ti 0.01 - 0.05%, B 0.0005 - 0.003%, V 0.02 - 0.10%, Nb less than 0.3%, Ni less than 1%, Cu less than 0.5%, the remainder being iron and unavoidable impurities.
- the patent describes direct quenched martensitic sheet-like steels which are temper annealed.
- European patent application np. EP 2,949,775 A1 discloses an ultra-high durability steel plate having a low yield ratio, comprising the chemical elements in mass percentages of: C: 0.18-0.34%, Si: 0.10-0.40%, Mn: 0.50-1.40%, Cr: 0.20-0.70%, Mo: 0.30-0.90%, Nb: 0-0.06%, Ni: 0.50-2.40%, V: 0-0.06%, Ti: 0.002-0.04%, Al: 0.01-0.08%, B: 0.0006-0.0020%, N ⁇ 0.0060%, O ⁇ 0.0040%, Ca: 0-0.0045%, and the balance of Fe and other unavoidable impurities.
- a process of manufacturing the steel plate is also disclosed, wherein the heating temperature is 1080-1250 °C; the quenching temperature is 860-940 °C; and the tempering temperature is 150-350 °C.
- Japanese patent application no. JP 2006206942A provides a method of manufacturing a high-tensile steel excellent in hydrogen embrittlement resistance, which is less likely to cause hydrogen embrittlement such as delayed fracture, weld delayed cracking, and sulphide corrosion cracking.
- the steel is composed of, in mass%, C: 0.02 to 0.25%, Si: 0.01 to 0.8%, Mn: 0.5 to 2.0%, Al: 0.005 to 0.1%, N: 0.0005 to 0.008%, P: 0.03% or less, S : 0.03% or less, optionally containing one or two or more of Cu, Ni, Cr, Mo, Nb, V, Ti, B, Ca, REM, Mg, and the balance being Fe and unavoidable impurities.
- Such flat steel products may be used for applications, such as wear or structural applications, in which the steel must exhibit high strength in combination with sufficient hardness, bendability and impact toughness both in the as-produced steel products and in the HAZ (heat affected zone) area of welded steel products.
- HAZ heat affected zone
- An object of the invention is to provide improved hot-rolled steel.
- Carbon is needed to achieve high base material strength and the other elements listed above promote the strength of the weld so as to avoid softened zones in a welded seam which would "catch" the fracture.
- Manganese, molybdenum and vanadium also promote the strength of quenched and tempered steel.
- each element in the embodiments a) to d) provides a good combination of toughness and high strength.
- Hot-rolled steel having the chemical composition given above and manufactured using the method described herein exhibits high strength (i.e. a yield strength (Rp 0.2 ) of at least 1100 MPa) along and transverse to a rolling direction and a tensile strength of at least 1120 MPa along and transverse to a rolling direction, good bendability (i.e.
- a minimum bending radius of 5.0 x thickness along and/or transverse to a rolling direction preferably 4.0 x thickness along a rolling direction or more preferably 3.5 x thickness along a rolling direction and an impact toughness of at least 34 J/cm 2 and more, preferably an impact toughness of at least 50 J/cm 2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -40°C longitudinally to the rolling direction, and good ductility (i.e. an A%-elongation of at least 8% along and transverse to the rolling direction, preferably of at least 10% or most preferably at least 12%).
- Mechanical properties are defined according to the testing instructions of standard ISO 10025-6.
- this combination of properties is achieved both in the as-produced hot-rolled quenched and tempered steel products and in the HAZ (heat affected zone) area of welded hot-rolled steel products (which are welded using a filler material that is designed for steels having a yield strength of at least 1100 MPa, preferably of at least 960 MPa, more preferably at least 900 MPa, most preferably of at least 890 MPa, such as X90 or preferably X96).
- the prior art includes hot-rolled steel sheets having a yield strength (Rp 0.2 ) of at least 1100 MPa, although those prior art hot-rolled steel sheets do not have such good weldability or such good mechanical properties when welded.
- hot-rolled steel as used herein means a steel that is hot-rolled to be sheet-like, such as a hot-rolled heavy plate or preferably hot-rolled strip steel.
- the thickness of the hot-rolled strip steel may be 2 - 15 mm, preferably 2.5 - 10 mm.
- the thickness of the hot-rolled heavy plate may be 4 - 50 mm, preferably 5 - 25 mm.
- the hot-rolled steel comprises 0.4-1.7 mass-% Cr, preferably 1.0 -1.7 mass-% Cr.
- the chemical composition contains both Ni and Cu, and the amount of Ni ⁇ 0.33 x the amount of Cu, preferably the amount of Ni ⁇ 0.5 x the amount of Cu so as to maintain high surface quality of the steel in hot-rolling.
- the alloying costs of the hot-rolled steel can be kept as low as possible while achieving the advantageous properties of the hot-rolled steel according to the present invention (since Nickel is an expensive alloying element).
- Nickel prevents Copper from melting under the scale that may be formed on the outer surfaces of the steel when it is annealed before hot-rolling and which comprises iron oxides and thereby prevents Copper from going into the grain boundaries, which can weaken the grain boundaries. Weakened grain boundaries can promote surface cracking and defects during the hot-rolling process.
- the chemical composition contains both Ni and Cu in a total amount of at least 0.5 mass-%, or at least 1.0 mass-%, or at least 1.2 mass-%.
- the hot-rolled steel has a tensile strength of at least 1120 MPa, or at least 1130 MPa, or at least 1200 MPa, and/or maximum 1250 MPa or maximum 1300 MPa, or maximum up to 1450 MPa along and/or transverse to the rolling direction.
- the hot-rolled steel i is used for metal active gas (MAG) welded with reinforcement, as defined in claim 13.
- MAG metal active gas
- the t8/5 time is the time it takes for a weld seam and an adjacent heat-affected zone (HAZ) to cool from 800°C to 500°C.
- welding seam means the total weld area (WM and HAZ).
- a t8/5 time lower than 5 seconds may adversely affect the toughness properties of the steel.
- a t8/5 time greater than 20 seconds may adversely affect the strength of the steel.
- the MAG-welded transversal tensile test specimen's fracture does not occur in the weld metal or fusion line and the fracture is moved ⁇ 1 mm or ⁇ 2 mm or ⁇ 3 mm from the fusion line with or without reinforcement when using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds.
- the hot-rolled steel has an elongation of at least 7%, preferably at least 8%, more preferably at least 9% when a tensile test is carried out across a weld seam of a welded hot-rolled steel product where the weld is longitudinal to the rolling direction.
- the hot-rolled steel is welded using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds..
- the present invention also concerns a method for manufacturing hot-rolled steel according to any of the embodiments of the invention, having the features recited in claim 8.
- the method comprises the following steps carried out in the following order:
- Quenching results in at least 90% martensite in the microstructure, preferably 95% martensite, and more preferably 99% martensite when the microstructure is examined in 1 ⁇ 4 thickness.
- the quenching step is preferably a direct quenching step, which is for example conducted a maximum of 15 seconds after the last hot-rolling pass.
- the cooling rate during quenching is typically 30 - 150 °C/s.
- the method comprises the step of temper annealing at a temperature of 500 - 650 °C, more preferably 550 - 650 °C, whereby the tempering time is 1 hour or more, or temper annealing at a temperature of 500 - 750 °C, more preferably 550 - 750 °C, if the tempering time is less than 1 hour.
- Tempering time is the holding time after the steel has reached the tempering temperature. The temper annealing improves the impact toughness and elongation of the hot-rolled steel while maintaining its strength.
- the temper annealing step is carried out at a temperature of 150 - 499°C, more preferably 180 - 250°C with any tempering time used.
- the microstructure of the hot-rolled steel before the temper annealing step contains at least 90% martensite, preferably at least 95% martensite and more preferably at least 99% martensite when said microstructure is examined in 1 ⁇ 4 thickness.
- the temper annealing step may be conducted immediately after the quenching.
- one or more additional method steps may be carried out between the quenching step and the temper annealing step.
- the quenched steel may be subjected to an acid pickling step and/or coiling and/or straightening.
- the mechanical properties of the hot-rolled steel as produced and when welded are good because of the chemical composition of the steel and because the material is tempered at a relatively high temperature of at least 500°C, preferably of at least 550°C and more preferably of at least 580°C. If the tempering time is relatively short, i.e. less than 1 hour, (for example when induction tempering is used), the tempering temperature can be higher, for example 50°C higher or more. The maximum tempering temperature is 750°C.
- the temper annealing is preferably carried out in a furnace other than a bell-type furnace, i.e. the temper annealing step is preferably not carried out in a bell-type furnace but any other suitable type of furnace.
- a bell-type furnace is a batch furnace that consists of an insulated chamber with a steel shell and a heating system. Bell furnaces have removable covers called bells, which are lowered over the load and hearth using a crane. An inner bell is placed over the hearth and sealed to supply a protective atmosphere. An outer bell is lowered to provide the heat supply.
- the steel may typically be subjected to a temperature of 450-600°C for a long period of time since the temperature inside the insulated chamber rises and falls slowly, which may cause brittleness in some steels since atomic segregations may form at grain boundaries, which can weaken the steels and make them very fragile at room temperature.
- the method comprises the step of strip rolling the hot-rolled steel.
- the hot-rolled steel comprises a maximum of 0.005 mass-% Niobium and ⁇ 0.15 mass-% Carbon when the hot-rolled steel is strip rolled.
- the hot-rolled steel comprises a minimum of 0.005 or 0.04 or 0.02 mass-% Niobium when the hot-rolled steel is not strip rolled. More than 0.06 mass-% Niobium has no effect or only a minor effect on the strength properties of the hot-rolled steel.
- the strip rolling as a process produces a more elongated austenite grain structure (flattened) compared to plate rolling, where the time for recrystallization is longer and recrystallization is easier.
- the flattening ratio can be increased.
- the plate steel is often alloyed with Niobium. Flattening of austenite increases the strength and impact toughness of the steel.
- Niobium When steel is reheated and quenched after hot-rolling, Niobium is needed to get high strength and impact strength.
- the minimum amount of Niobium required is then >0.005 mass-%, preferably >0.02 mass-%.
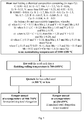
- Figure 1 shows the steps of a method for manufacturing hot-rolled steel according to any of the embodiments of the invention having a chemical composition containing (in mass-%):
- the method comprises the step of heating a steel slab having the chemical composition described above to an austenitizing temperature of 1000-1350 °C.
- the thickness of the steel slab is, for example, 210 mm and it is preferably heated to an austenitizing temperature of 1200 - 1350°C, where it is kept until it is of adequately even warmth and the alloying elements have adequately dissolved into the matrix. Typically, this takes several hours. If the austenitizing temperature is below 1200 °C, there can be a danger that not all of the alloying elements will dissolve into the austenite, i.e. the austenite is not made homogenous and during the tempering, the precipitation hardening may remain at a low level. On the other hand, if the austenitizing temperature is higher than 1350 °C, this will result in an exceptionally large grain size of the austenite and increased oxidation of the slab surface. Annealing time in reheating is typically varied in the range of 2 - 4 hours, but, depending on the selected furnace technology and the thickness of the slab, it can also be longer than 4 hours or shorter than 2 hours.
- hot-rolling is conducted, which may typically comprise a roughing step and a subsequent finish rolling step.
- the temperature of hot-rolling at the last pass is 760 - 1050°C.
- the finishing rolling temperature at the last pass of the hot-rolling is 760 - 960°C.
- the end temperature of hot-rolling is preferably above 830 °C or more preferably at least 850°C so that rolling forces remain reasonable, and at the most 940 °C, and more preferably 920° at the most, wherein i.a. excellent surface quality is assured.
- the steel is quenched, i.e. cooled at an accelerated cooling rate, typically of 30 - 150 °C/s, using one step cooling for example, preferably at a maximum cooling rate of 120°C/s, in a suitable quenching medium, such as water or oil, to a temperature of 300 °C or less, or preferably 150°C or less, i.e. any temperature between room/ambient temperature and 300°C. If it is a strip product it is coiled at that temperature, i.e. at a coiling temperature of 300°C or less.
- the quenching is direct quenching conducted a maximum of 15 seconds after the last hot-rolling pass.
- the end temperature of quenching is a maximum of 150°C, because, in this case, after quenching, a steel product with good flatness is achieved.
- the quenched steel is subsequently subjected to temper annealing at a temperature of 500 - 650 °C if the tempering time is 1 hour or more, or temper annealing at a temperature of 500 - 750 °C if the tempering time is less than 1 hour.
- the tempering temperature is 400 - 750°C then the temper annealing is typically carried out in a furnace other than a bell-type furnace so as to avoid the risk of adversely affecting the strength and toughness properties of the steel.
- the tempering temperature is 150 - 250°C then the tempering annealing may also be carried out in a bell-type furnace without adversely affecting the strength and toughness properties of the steel and to minimize production costs.
- Tempering at annealing temperatures of 250 - 400°C is not recommended due to low temperature tempering embrittlement if good toughness properties are required. Typically, higher temperatures promote good total elongation values, and lower tempering temperatures promote higher strength properties.
- the Larsen Miller parameter, P is between 15 - 19.5, and preferably 16 - 18.
- the temper annealing step may be carried out on quenched steel, such as steel sheet cut from a coil, or on a steel sheet that is continuously unwound from a coil, or a heavy plate.
- the temper annealing step may alternatively be carried out on a whole coil, for example in a bell type furnace.
- the microstructure of the hot-rolled steel before the temper annealing step contains at least 90% martensite, preferably at least 95% martensite and more preferably at least 99% martensite when the microstructure is examined in 1 ⁇ 4 thickness.
- the majority of the microstructure will be martensite although it may contain some bainite.
- the content of ferrite and pearlite before the temper annealing step must be in total less than 10%, preferably less than 5%.
- Manganese content as a percentage by weight is 1.1 - 2.2 mass-% in order to assure good hardenability in the weld metal and HAZ of welded hot-rolled steel. Manganese also promotes hardenability of the base material during the quenching step.
- the expression "weld metal” is intended to mean the part of the weld seam that consists mainly of filler material.
- Molybdenum precipitates in temper annealing, which decreases the lowering of strength caused by tempering treatment and thus helps in achieving high strength. Additionally, Molybdenum is used inter alia to prevent the brittleness of steel by slowing infiltration of inter alia Phosphorus into the grain boundaries during temper annealing. Molybdenum also efficiently increases the hardenability of the base material and ensures good strength properties of welded seams of welded hot-rolled steel.
- Niobium may decrease the bendability of a hot-rolled steel if it is present in a large amount.
- the use of Niobium as an alloying element is however of advantage in achieving adequate strength and impact toughness in hot-rolled steel.
- Niobium promotes smaller grain size in steel, which results in better properties of the steel.
- Niobium may be needed, especially in the case of heavy plate, to enable smaller amounts of other alloying elements that promote good strength and toughness properties to be used.
- the steel can be also made without using Niobium.
- Niobium is therefore an optional alloying element in the hot-rolled steel according to the present invention, the content of which should be limited to 0.06 mass-%, preferably to 0.04 mass-%, and more preferably to 0.005 mass-%, wherein the best possible bendability properties for the hot-rolled steel are assured.
- Titanium is an optional alloying element in the hot-rolled steel according to the present invention, which may be required for binding Nitrogen in the steel, and so that Boron functions efficiently as an improver of hardenability and does not form Boron nitrides. Titanium is used, because it works more reliably with quenched steel than Aluminium.
- the Titanium content is 0 - 0.15 mass-%, preferably 0 - 0.05 mass-% and more preferably 0.005 - 0.02 mass-%. Titanium nitrides exhibit grain growth in the heat affected zone of a weld and improve the toughness properties of a welded seam.
- TiN may increase, which is detrimental in terms of the impact toughness and bending properties of the hot-rolled steel.
- the Ti/N ratio of the hot-rolled steel is preferably in the range 3 - 4.
- larger Titanium contents up to 0.15 mass-% may be used to increase strength in the as-tempered condition.
- Vanadium content in the hot-rolled steel according to the present invention must be more than 0.1 mass-% and ⁇ 0.25 mass-%, preferably more than 0.10 and ⁇ 0.20 mass-%, or at least 0.11 mass-% Vanadium, or at least 0.12 mass-% Vanadium, or at least 0.13 mass-% Vanadium, or at least 0.14 mass-% Vanadium in order to assure high strength. It has however been found that a too high amount of Vanadium is detrimental to the impact toughness of the quenched and tempered steel. The amount of Vanadium should not therefore exceed 0.25 mass-%. Vanadium has a strong precipitation strengthening effect after tempering and is needed to achieve high strength both in base metal and in the HAZ.
- Aluminium is used to condense steel, i.e. to bind oxygen from the steel.
- the Aluminium content is 0.01 - 0.15 mass-%, preferably 0.015 - 0.08 mass-% to prevent excessive formation of aluminium oxides.
- Boron is an effective alloying element that promotes hardenability of the steel in quenching. It is an essential alloying element in this invention since it promotes strength and hardness properties in the weld metal and heat-affected zone (HAZ).
- HZ heat-affected zone
- Boron moves from the base material to the weld metal, thereby increasing the hardness of the weld metal. This ensures that fracture does not occur in the weld metal or fusion line. Fracture can be moved as far as possible away from the fusion line towards the base material in high static loads.
- the Boron content is 0.0005 - 0.010 mass-%, preferably 0.0005 - 0.005 mass-% and more preferably 0.001 - 0.003 mass-%.
- a Boron content of at least 0.0005 mass-% promotes hardenability of the base material and of the HAZ, ensuring good strength properties.
- a Boron content of more than 0.005 mass-% is worthless as regards the hardenability of the base material and the HAZ.
- the Boron content is more than 0.001 mass-%, it ensures matching strength properties of the weld and fracture location as previously described.
- a Boron content of more than 0.010 mass-% can be detrimental for mechanical properties of the steel.
- the Chromium content of hot-rolled steel according to the present invention is 0. 1 - 1.7 mass-%, preferably 0.4 - 1.7 or 0.6 - 1.5 mass-%, or more than 1.0 mass-% in order to achieve high strength and good hardenability both in the hot-rolled steel as produced and in the HAZ of a welded hot-rolled steel product. Chromium also promotes tempering resistance.
- the chemical composition of hot-rolled steel according to the present invention contains both Ni and Cu in a total amount of at least 0.5 mass-%, or at least 1.0 mass-%, or at least 1.2 mass-%.
- Copper is an optional alloying element. It can be used in an amount up to 1.5 mass-%, preferably 0.1-1.0 mass-% in order to increase the strength or improve the weather resistance of the hot-rolled steel.
- the chemical composition contains both Ni and Cu, and the amount of Ni ⁇ 0.33 x the amount of Cu, preferably the amount of Ni ⁇ 0.5 x the amount of Cu.
- Cr+Cu+Ni is between 0.4 - 5.7, preferably between 1.4 - 3.5 and more preferably between 2 - 3.
- Nickel is an essential alloying element in the hot-rolled steel according to the present invention and it improves the toughness of the heat-affected zones and the weld metal of welded seams and it also improves the surface quality of the hot-rolled steel containing Copper but may, under some circumstances, slightly decrease the impact toughness of the tempered steel.
- Phosphorus weakens the impact toughness of quenched and tempered steel and the Phosphorus content should therefore be limited to a maximum of 0.015 mass-%, preferably to a maximum of 0 - 0.009 mass-%.
- Sulphur content is limited to a maximum of 0.008 mass-%, preferably to a maximum of 0.004 mass-%, to assure good impact toughness and formability in the hot-rolled steel according to the present invention.
- Zirconium is an optional alloying element that may replace Niobium if needed.
- the Zirconium content can be between 0 - 0.2 mass-%, preferably 0 - 0.01 mass-%.
- Calcium is an optional alloying element that may be used to modify the morphology of inclusions in the steel.
- the Calcium content can be between 0 - 0.004 mass-%. If the amount of Calcium exceeds 0.004 mass-% the inclusions in the steel may be too large, which may adversely affect the physical properties of the steel.
- the hot-rolled steel has a tensile strength of at least 1120 MPa and up to 1450 MPa.
- the hot-rolled steel has an A%-elongation of at least 8% (i.e. permanent elongation of length, expressed in percent of length) or even of at least 10% or at least 12% along and transverse to the rolling direction.
- the hot-rolled steel has such an elongation in its as-produced condition.
- the hot-rolled steel also has an elongation of at least 7%, preferably at least 8%, more preferably at least 9% when a tensile test is carried out across a weld seam of a welded hot-rolled steel product where the weld is longitudinal to the rolling direction.
- the hot-rolled steel an impact toughness of at least 34 J/cm 2 and more preferably an impact toughness of at least 50 J/cm 2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -20°C and more preferably at -40°C longitudinally and transverse to the rolling direction.
- the hot-rolled steel has such an impact strength in its as-produced condition.
- the hot-rolled steel is metal active gas (MAG) welded with our without reinforcement, using a V- or Y-groove welding method, whereby a first pass is welded from a bottom or top side, preferably from a bottom side, and other passes from a top side, using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds, which may be determined by welding the hot-rolled steel and measuring the time it takes for the weld seam and the adjacent heat-affected zone (HAZ) to cool from 800°C to 500°C.
- MAG metal active gas
- the hot-rolled steel has a minimum bending radius of 5.0 x thickness or more preferably a minimum bending radius of 4.0 x thickness or more preferably a minimum bending radius of 3.5 x thickness longitudinally and transverse to the rolling direction.
- the steel has a minimum bending radius of 5.0 x thickness or preferably a minimum bending radius of 4.0 x thickness or more preferably a minimum bending radius of 3.5 x thickness longitudinally to the rolling direction, and a minimum bending radius of 5.0 x thickness transverse to the rolling direction.
- the hot-rolled steel according to the present invention is suitable for applications, such as wear or structural applications, in which the steel must exhibit high strength in combination with sufficient hardness, bendability and impact toughness both in the as-produced products and in the HAZ (heat affected zone) of welded hot-rolled steel products.
- the hot-rolled steel according to the present invention may be used to produce any component for construction, mining, material-handling, earth-moving, pile driving, snow-plowing, landscaping or rock drilling equipment.
- the hot-rolled steel may for example be used to produce a lifting boom for an excavator or crane.
- compositions labelled “INV” in Table 1 are steels that have the chemical composition and the physical properties of steel according to the present invention and which have been manufactured using a method according to the present invention. Comparative examples that do not have the chemical composition or the physical properties of steel according to the present invention, or which have not been manufactured using a method according to the present invention are labelled “REF” in Table 1.
- Table 1 Chemical compositions Comp.
- Table 2 Process parameters composition process tempering thickness furnT FRT CT T t I NV/REF code code code code mm °C °C °C min A1 R02 S600 8.0 1280 856 50 600 30 INV B R04 S600 8.0 1280 862 50 600 30 REF c R06 S560 8.0 1280 878 50 560 30 INV A2 R12 S600 4.0 1278 924 50 600 15 INV A2 R13 S585 8.0 1267 871 50 585 15 INV A2 R13 S600 8.0 1267 871 50 600 15 INV A3 R14 S585 6.0 1279 897 50 585 15 INV A3 R14 S600 6.0 1279 897 50 600 15 INV A2 R16 S585 4.0 1279 917 50 585 15 INV A2 R16 S600 4.0 1279 917 50 600 15 INV D B05 C420 6.0 1250 919 100 420 720 REF A1 B09 C200 8.0
- Bending tests were carried out using three-point bending with samples having an area of 300 x 300 mm 2 . Samples were bent to an angle of 90° with one press and all samples were bent into a Z-shape so that both the upper and lower surfaces of the samples were tested. Mechanical properties and bendability of the samples were tested both longitudinally with respect to the rolling direction, and transversely with respect to the rolling direction.
- Welding tests were carried out using a metal active gas (MAG) welding method and V- and Y -grooves.
- the welding consumables used were according to standard ENG 89 5 M21 Mn4Ni2.5CrMo (Commercial grade X96). The first pass was welded from bottom or top side, preferably from the bottom side, and others passes were welded from the top side.
- Welding consumables having a tensile strength of 960 MPa were used and t8/5 was varied between 6 - 18 seconds. Tensile tests across the weld showed that the weld had a yield strength of 1100 MPa (Rp0.2) and the fracture was located at the base metal (BM).
- the target was to achieve a combination of strength and toughness properties which are as good as possible in the weld so that matching tensile properties can be achieved without losing toughness.
- the aim was to obtain a fracture in a static tensile test over the weld that is located as far as possible from the weld metal (WM) and fusion line (FL), which enables extremely good elongation to fracture values for the welded structure.
- the behaviour of a welded structure is predictable and safe when the fracture in static loading takes place as far as possible away from the WM and FL and the elongation to fracture is high.
- the inventors have found that steels according to the present invention can fulfill these requirements even if the yield strength for the base material is more than 1100 MPa.
- known steels with such a high strength have a fracture located over the weld (WM or FL) when a tensile test is performed, especially when un-matching welding consumables are used (the yield strength of un-matching welding consumables is typically less than 1100 MPa).
- Table 4 shows the welding parameters that were used in the tests and the test results obtained.
- Steels according the invention have a fracture that is located at a distance from the weld (WM and/or FL) when a static load in a tensile test is set over the weld. It is surprising compared to known steels that such behaviour can be achieved with or even without reinforcement. Without reinforcement, the achievement of such behaviour is very innovative. Fracture location is labelled “BM” in Table 4 when the fracture is in the base material, "HAZ” when it occurs in the Heat Affected Zone, and "WM” when the fracture occurs in the Weld Metal.
- Figures 2 and 3 shows typical hardness profiles over the welded seam tested near the face side and the root side of the welded samples. It is surprising that steels according to the present invention can have a very smooth hardness profile over the weld and that there are no soft zones that could start to neck during a tensile test and thereby influence the location of the fracture. Normally, steels with a yield strength of 1100 MPa welded with un-matching welding consumables (X90 and/or X96) exhibit some softening in the HAZ and especially in the WM. Steel according to the invention can maintain good hardness in the HAZ but also have good hardness in the WM due to the diffusion of alloying elements promoting hardening (i.e. Boron). Low carbon content in the steels according to the invention (i.e. 0.1 - 0.20 mass-% Carbon) ensures that a weld has high toughness as well as good hardness.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Sheet Steel (AREA)
Description
- The present invention concerns high strength hot-rolled steel and a method for manufacturing such hot-rolled steel.
- Martensitic flat steel products have for many years been manufactured using a method comprising the steps of heating a steel slab to an austenitizing temperature, hot-rolling, re-heating, quenching and tempering, or alternatively, heating a steel slab to an austenitizing temperature, hot-rolling, direct quenching and tempering.
- For example, European patent no.
EP 2,576,848 discloses a method for producing a hot-rolled steel from a steel, whose composition as percentages by weight is C 0.075 - 0.12%, Si 0.1 - 0.8%, Mn 0.8 - 1.7%, Al 0.015 - 0.08%, P less than 0.012%, S less than 0.005%, Cr 0.2 - 1.3%, Mo 0.15 - 0.80%, Ti 0.01 - 0.05%, B 0.0005 - 0.003%, V 0.02 - 0.10%, Nb less than 0.3%, Ni less than 1%, Cu less than 0.5%, the remainder being iron and unavoidable impurities. The patent describes direct quenched martensitic sheet-like steels which are temper annealed. The hot-rolled steel is exceptionally temper-resistant after the direct quenching process, wherein by tempering, high-strength (i.e. Rp0.2 of at least 890MPa) combined with good impact toughness (Charpy V (-20°C) =37J) and flangeability, as well as good weldability are achieved. - European patent application np.
EP 2,949,775 A1 discloses an ultra-high durability steel plate having a low yield ratio, comprising the chemical elements in mass percentages of: C: 0.18-0.34%, Si: 0.10-0.40%, Mn: 0.50-1.40%, Cr: 0.20-0.70%, Mo: 0.30-0.90%, Nb: 0-0.06%, Ni: 0.50-2.40%, V: 0-0.06%, Ti: 0.002-0.04%, Al: 0.01-0.08%, B: 0.0006-0.0020%, N ¤0.0060%, O ¤0.0040%, Ca: 0-0.0045%, and the balance of Fe and other unavoidable impurities. A process of manufacturing the steel plate is also disclosed, wherein the heating temperature is 1080-1250 °C; the quenching temperature is 860-940 °C; and the tempering temperature is 150-350 °C. - Japanese patent application no.
JP 2006206942A - Such flat steel products may be used for applications, such as wear or structural applications, in which the steel must exhibit high strength in combination with sufficient hardness, bendability and impact toughness both in the as-produced steel products and in the HAZ (heat affected zone) area of welded steel products.
- An object of the invention is to provide improved hot-rolled steel.
- This object is achieved by hot-rolled steel having the features recited in claim 1,
- By adding the alloying elements in the recited amounts, a combination of good base material toughness and strength properties can be achieved and any fracture occurring during a tensile test of a weld will occur as far as possible from the fusion line.
- Carbon is needed to achieve high base material strength and the other elements listed above promote the strength of the weld so as to avoid softened zones in a welded seam which would "catch" the fracture. Manganese, molybdenum and vanadium also promote the strength of quenched and tempered steel.
- From a toughness point of view, it is important to have a carbon content that is as low as possible. The amount of each element in the embodiments a) to d) provides a good combination of toughness and high strength.
- Hot-rolled steel having the chemical composition given above and manufactured using the method described herein exhibits high strength (i.e. a yield strength (Rp0.2) of at least 1100 MPa) along and transverse to a rolling direction and a tensile strength of at least 1120 MPa along and transverse to a rolling direction, good bendability (i.e. a minimum bending radius of 5.0 x thickness along and/or transverse to a rolling direction, preferably 4.0 x thickness along a rolling direction or more preferably 3.5 x thickness along a rolling direction and an impact toughness of at least 34 J/cm2 and more, preferably an impact toughness of at least 50 J/cm2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -40°C longitudinally to the rolling direction, and good ductility (i.e. an A%-elongation of at least 8% along and transverse to the rolling direction, preferably of at least 10% or most preferably at least 12%). Mechanical properties are defined according to the testing instructions of standard ISO 10025-6.
- Preferably, this combination of properties is achieved both in the as-produced hot-rolled quenched and tempered steel products and in the HAZ (heat affected zone) area of welded hot-rolled steel products (which are welded using a filler material that is designed for steels having a yield strength of at least 1100 MPa, preferably of at least 960 MPa, more preferably at least 900 MPa, most preferably of at least 890 MPa, such as X90 or preferably X96).
- The prior art includes hot-rolled steel sheets having a yield strength (Rp0.2) of at least 1100 MPa, although those prior art hot-rolled steel sheets do not have such good weldability or such good mechanical properties when welded.
- The expression hot-rolled steel as used herein means a steel that is hot-rolled to be sheet-like, such as a hot-rolled heavy plate or preferably hot-rolled strip steel. The thickness of the hot-rolled strip steel may be 2 - 15 mm, preferably 2.5 - 10 mm. The thickness of the hot-rolled heavy plate may be 4 - 50 mm, preferably 5 - 25 mm. According to an embodiment of the invention the hot-rolled steel comprises 0.4-1.7 mass-% Cr, preferably 1.0 -1.7 mass-% Cr.
- According to an embodiment of the invention the chemical composition contains both Ni and Cu, and the amount of Ni ≥ 0.33 x the amount of Cu, preferably the amount of Ni ≥ 0.5 x the amount of Cu so as to maintain high surface quality of the steel in hot-rolling. Furthermore, the alloying costs of the hot-rolled steel can be kept as low as possible while achieving the advantageous properties of the hot-rolled steel according to the present invention (since Nickel is an expensive alloying element). Nickel prevents Copper from melting under the scale that may be formed on the outer surfaces of the steel when it is annealed before hot-rolling and which comprises iron oxides and thereby prevents Copper from going into the grain boundaries, which can weaken the grain boundaries. Weakened grain boundaries can promote surface cracking and defects during the hot-rolling process.
- According to an embodiment of the invention the chemical composition contains both Ni and Cu in a total amount of at least 0.5 mass-%, or at least 1.0 mass-%, or at least 1.2 mass-%.
- According to an embodiment of the invention the hot-rolled steel has a tensile strength of at least 1120 MPa, or at least 1130 MPa, or at least 1200 MPa, and/or maximum 1250 MPa or maximum 1300 MPa, or maximum up to 1450 MPa along and/or transverse to the rolling direction.
- According to an embodiment of the invention the hot-rolled steel iis used for metal active gas (MAG) welded with reinforcement, as defined in claim 13.
- The t8/5 time is the time it takes for a weld seam and an adjacent heat-affected zone (HAZ) to cool from 800°C to 500°C. The expression "weld seam" means the total weld area (WM and HAZ). A t8/5 time lower than 5 seconds may adversely affect the toughness properties of the steel. A t8/5 time greater than 20 seconds may adversely affect the strength of the steel. The MAG-welded transversal tensile test specimen's fracture does not occur in the weld metal or fusion line and the fracture is moved ≥ 1 mm or ≥ 2 mm or ≥ 3 mm from the fusion line with or without reinforcement when using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds..
- According to the embodiment defined in claim 7 the hot-rolled steel has an elongation of at least 7%, preferably at least 8%, more preferably at least 9% when a tensile test is carried out across a weld seam of a welded hot-rolled steel product where the weld is longitudinal to the rolling direction. The hot-rolled steel is welded using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds..
- The present invention also concerns a method for manufacturing hot-rolled steel according to any of the embodiments of the invention, having the features recited in
claim 8. - The method comprises the following steps carried out in the following order:
- heating a steel slab having a chemical composition as recited in claim 1 to an austenitizing temperature of 1000 - 1350 °C, preferably 1200 - 1350°C,
- hot-rolling such that a finishing rolling temperature is 760 - 1050°C, preferably 760 - 960°C,
- quenching to 300 °C or less, preferably 150°C or less, and
- Quenching results in at least 90% martensite in the microstructure, preferably 95% martensite, and more preferably 99% martensite when the microstructure is examined in ¼ thickness.
- It is beneficial to use such relatively high austenitizing temperatures because in strip rolling the final thickness is small and steel tends to cool down during rolling. By using higher heating temperatures, steel is warmer during strip rolling and rolling forces are smaller. Austenite grain refinement is also easier then. Higher austenitization temperatures also promote more uniform grain structure before rolling.
- If very high temperatures (of more than 1350°C) are used there is a risk that large grain size will be obtained. Furthermore, steel may oxidize aggressively and there may be a yield loss due to high scaling. Additionally, production costs will be increased.
- The quenching step is preferably a direct quenching step, which is for example conducted a maximum of 15 seconds after the last hot-rolling pass. The cooling rate during quenching is typically 30 - 150 °C/s.
- For maximizing total elongation in a direction transverse to the rolling direction, the method comprises the step of temper annealing at a temperature of 500 - 650 °C, more preferably 550 - 650 °C, whereby the tempering time is 1 hour or more, or temper annealing at a temperature of 500 - 750 °C, more preferably 550 - 750 °C, if the tempering time is less than 1 hour. Tempering time is the holding time after the steel has reached the tempering temperature. The temper annealing improves the impact toughness and elongation of the hot-rolled steel while maintaining its strength. When maximum total elongation is not required, the temper annealing step is carried out at a temperature of 150 - 499°C, more preferably 180 - 250°C with any tempering time used. The microstructure of the hot-rolled steel before the temper annealing step contains at least 90% martensite, preferably at least 95% martensite and more preferably at least 99% martensite when said microstructure is examined in ¼ thickness.
- It should be noted that the temper annealing step may be conducted immediately after the quenching. Alternatively, one or more additional method steps may be carried out between the quenching step and the temper annealing step. For example, the quenched steel may be subjected to an acid pickling step and/or coiling and/or straightening.
- The mechanical properties of the hot-rolled steel as produced and when welded are good because of the chemical composition of the steel and because the material is tempered at a relatively high temperature of at least 500°C, preferably of at least 550°C and more preferably of at least 580°C. If the tempering time is relatively short, i.e. less than 1 hour, (for example when induction tempering is used), the tempering temperature can be higher, for example 50°C higher or more. The maximum tempering temperature is 750°C.
- According to an embodiment of the invention the temper annealing is preferably carried out in a furnace other than a bell-type furnace, i.e. the temper annealing step is preferably not carried out in a bell-type furnace but any other suitable type of furnace. A bell-type furnace is a batch furnace that consists of an insulated chamber with a steel shell and a heating system. Bell furnaces have removable covers called bells, which are lowered over the load and hearth using a crane. An inner bell is placed over the hearth and sealed to supply a protective atmosphere. An outer bell is lowered to provide the heat supply. If temper annealing is carried out in a bell-type furnace, the steel may typically be subjected to a temperature of 450-600°C for a long period of time since the temperature inside the insulated chamber rises and falls slowly, which may cause brittleness in some steels since atomic segregations may form at grain boundaries, which can weaken the steels and make them very fragile at room temperature.
- According to an embodiment of the invention the method comprises the step of strip rolling the hot-rolled steel. The hot-rolled steel comprises a maximum of 0.005 mass-% Niobium and < 0.15 mass-% Carbon when the hot-rolled steel is strip rolled.
- The hot-rolled steel comprises a minimum of 0.005 or 0.04 or 0.02 mass-% Niobium when the hot-rolled steel is not strip rolled. More than 0.06 mass-% Niobium has no effect or only a minor effect on the strength properties of the hot-rolled steel.
- When direct quenched, the strip rolling as a process produces a more elongated austenite grain structure (flattened) compared to plate rolling, where the time for recrystallization is longer and recrystallization is easier. By using Niobium, the flattening ratio can be increased. To achieve the same flattening ratio as for strip rolling, the plate steel is often alloyed with Niobium. Flattening of austenite increases the strength and impact toughness of the steel.
- When steel is reheated and quenched after hot-rolling, Niobium is needed to get high strength and impact strength. The minimum amount of Niobium required is then >0.005 mass-%, preferably >0.02 mass-%.
- The present invention will hereinafter be further explained by means of non-limiting examples with reference to the appended figures where;
-
Figure 1 shows a flow chart showing the steps of a method according to an embodiment of the invention, including the alternative to temper anneal at at temperature of 150-499°C falling outside the embodiment. -
Figure 2 shows hardness profiles for material having a thickness of 8 mm over the weld tested from face side (i.e. the side at which welding took place) and the root side (i.e. the side opposite to the side at which welding took place), and -
Figure 3 shows hardness profiles for material having a thickness of 4 mm over the weld tested from face side and the root side. -
Figure 1 shows the steps of a method for manufacturing hot-rolled steel according to any of the embodiments of the invention having a chemical composition containing (in mass-%): - C 0.10 - 0.2, preferably 0.10 - 0.18, more preferably 0.12 - 0.18,
- Si 0 - 0.7, preferably 0.03 - 0.50, more preferably 0.10 - 0.30,
- Mn 1.3 - 2.2, preferably 1.4 - 1.8, more preferably 1.4 - 1.7,
- Nb 0 - 0.06, preferably 0 - 0.04, more preferably 0 - 0.005,
- Ti 0 - 0.15, preferably 0 - 0.05 more preferably 0.005 - 0.02,
- V more than 0.03 and ≤ 0.25, preferably more than 0.10 and ≤ 0.20,
- Al 0.01 - 0.15, preferably 0.015 - 0.08,
- B 0.0005 - 0.010, preferably 0.0005 - 0.005, more preferably 0.001 - 0.003,
-
Cr 0. 1 - 1.7, preferably 0.4 - 1.7 or 0.6 - 1.5, or more than 1.0 mass-%, - Mo 0.15 - 0.8, preferably 0.2 - 0.5,
- Cu 0 - 1.5, preferably 0.1-1.0,
- Ni 0.3 - 2.5, preferably 0.7 - 1.7,
- P 0 - 0.015, preferably 0 - 0.009,
- S 0 - 0.008, preferably 0 - 0.004,
- Zr 0 - 0.2, preferably 0 - 0.01
- Ca 0 - 0.004, preferably 0.001 - 0.003,
- preferably N 0-0.01 mass-%, more preferably ≤ 0.006 mass-%.
- balance Fe and unavoidable impurities.
- a) when 0.10 < C < 0.11 then Mn ≥ 1.6 and V > 0.14 and Mo ≥ 0.5 (in mass-%),
- b) when 0.11 < C < 0.125 then Mn ≥ 1.45 and V ≥ 0.13 and Mo ≥ 0.35 (in mass-%),
- c) when 0.125 < C < 0.15, then Mn ≥ 1.35 and V ≥ 0.12 and Mo ≥ 0.20 (in mass-%),
- d) when C ≥ 0.15 and V > 0.11, then Mn ≥ 1.3 and Mo ≥ 0.15 (in mass-%) or
when C ≥ 0.15 and V 0.03 - 0.11, then Mn > 1.3 and Mo > 0.15 and Nb > 0.02 and Cr+Cu+Ni >1.4 (in mass-%). - The method comprises the step of heating a steel slab having the chemical composition described above to an austenitizing temperature of 1000-1350 °C.
- The thickness of the steel slab is, for example, 210 mm and it is preferably heated to an austenitizing temperature of 1200 - 1350°C, where it is kept until it is of adequately even warmth and the alloying elements have adequately dissolved into the matrix. Typically, this takes several hours. If the austenitizing temperature is below 1200 °C, there can be a danger that not all of the alloying elements will dissolve into the austenite, i.e. the austenite is not made homogenous and during the tempering, the precipitation hardening may remain at a low level. On the other hand, if the austenitizing temperature is higher than 1350 °C, this will result in an exceptionally large grain size of the austenite and increased oxidation of the slab surface. Annealing time in reheating is typically varied in the range of 2 - 4 hours, but, depending on the selected furnace technology and the thickness of the slab, it can also be longer than 4 hours or shorter than 2 hours.
- After the heating step, hot-rolling is conducted, which may typically comprise a roughing step and a subsequent finish rolling step. The temperature of hot-rolling at the last pass is 760 - 1050°C. Preferably, the finishing rolling temperature at the last pass of the hot-rolling is 760 - 960°C. The end temperature of hot-rolling is preferably above 830 °C or more preferably at least 850°C so that rolling forces remain reasonable, and at the most 940 °C, and more preferably 920° at the most, wherein i.a. excellent surface quality is assured.
- After hot-rolling, or strip rolling, the steel is quenched, i.e. cooled at an accelerated cooling rate, typically of 30 - 150 °C/s, using one step cooling for example, preferably at a maximum cooling rate of 120°C/s, in a suitable quenching medium, such as water or oil, to a temperature of 300 °C or less, or preferably 150°C or less, i.e. any temperature between room/ambient temperature and 300°C. If it is a strip product it is coiled at that temperature, i.e. at a coiling temperature of 300°C or less. Preferably, the quenching is direct quenching conducted a maximum of 15 seconds after the last hot-rolling pass.
- This quenching gives the steel its exceptionally good mechanical properties including good impact toughness combined with good bendability. Preferably, the end temperature of quenching is a maximum of 150°C, because, in this case, after quenching, a steel product with good flatness is achieved.
- The quenched steel is subsequently subjected to temper annealing at a temperature of 500 - 650 °C if the tempering time is 1 hour or more, or temper annealing at a temperature of 500 - 750 °C if the tempering time is less than 1 hour. If the tempering temperature is 400 - 750°C then the temper annealing is typically carried out in a furnace other than a bell-type furnace so as to avoid the risk of adversely affecting the strength and toughness properties of the steel. However, if the tempering temperature is 150 - 250°C then the tempering annealing may also be carried out in a bell-type furnace without adversely affecting the strength and toughness properties of the steel and to minimize production costs. Tempering at annealing temperatures of 250 - 400°C is not recommended due to low temperature tempering embrittlement if good toughness properties are required. Typically, higher temperatures promote good total elongation values, and lower tempering temperatures promote higher strength properties.
- A suitable tempering treatment is defined by the formula P = T∗(20+logt), where the temperature T is in °K and the time is in hours. The Larsen Miller parameter, P, is between 15 - 19.5, and preferably 16 - 18.
- The temper annealing step may be carried out on quenched steel, such as steel sheet cut from a coil, or on a steel sheet that is continuously unwound from a coil, or a heavy plate. In the case of a strip product, the temper annealing step may alternatively be carried out on a whole coil, for example in a bell type furnace.
- The microstructure of the hot-rolled steel before the temper annealing step contains at least 90% martensite, preferably at least 95% martensite and more preferably at least 99% martensite when the microstructure is examined in ¼ thickness. The majority of the microstructure will be martensite although it may contain some bainite. The content of ferrite and pearlite before the temper annealing step must be in total less than 10%, preferably less than 5%.
- Manganese content as a percentage by weight is 1.1 - 2.2 mass-% in order to assure good hardenability in the weld metal and HAZ of welded hot-rolled steel. Manganese also promotes hardenability of the base material during the quenching step. The expression "weld metal" is intended to mean the part of the weld seam that consists mainly of filler material.
- The maximum Manganese content should be set according the equation so as to prevent excessive segregations and ensure good impact strength:
maximum Manganese content (in mass-%) = 2.7- 5∗Carbon content (in mass-%). - Molybdenum precipitates in temper annealing, which decreases the lowering of strength caused by tempering treatment and thus helps in achieving high strength. Additionally, Molybdenum is used inter alia to prevent the brittleness of steel by slowing infiltration of inter alia Phosphorus into the grain boundaries during temper annealing. Molybdenum also efficiently increases the hardenability of the base material and ensures good strength properties of welded seams of welded hot-rolled steel.
- It has been found that Niobium may decrease the bendability of a hot-rolled steel if it is present in a large amount. The use of Niobium as an alloying element is however of advantage in achieving adequate strength and impact toughness in hot-rolled steel. Niobium promotes smaller grain size in steel, which results in better properties of the steel. Niobium may be needed, especially in the case of heavy plate, to enable smaller amounts of other alloying elements that promote good strength and toughness properties to be used. In the case of a direct quenched strip product, the steel can be also made without using Niobium. Niobium is therefore an optional alloying element in the hot-rolled steel according to the present invention, the content of which should be limited to 0.06 mass-%, preferably to 0.04 mass-%, and more preferably to 0.005 mass-%, wherein the best possible bendability properties for the hot-rolled steel are assured.
- Titanium is an optional alloying element in the hot-rolled steel according to the present invention, which may be required for binding Nitrogen in the steel, and so that Boron functions efficiently as an improver of hardenability and does not form Boron nitrides. Titanium is used, because it works more reliably with quenched steel than Aluminium. The Titanium content is 0 - 0.15 mass-%, preferably 0 - 0.05 mass-% and more preferably 0.005 - 0.02 mass-%. Titanium nitrides exhibit grain growth in the heat affected zone of a weld and improve the toughness properties of a welded seam. On the other hand, at contents higher than 0.02 mass-%, the amount of relatively large-sized Titanium nitrides, TiN may increase, which is detrimental in terms of the impact toughness and bending properties of the hot-rolled steel. The Ti/N ratio of the hot-rolled steel is preferably in the range 3 - 4. However, larger Titanium contents up to 0.15 mass-% may be used to increase strength in the as-tempered condition.
- Vanadium content in the hot-rolled steel according to the present invention must be more than 0.1 mass-% and ≤ 0.25 mass-%, preferably more than 0.10 and ≤ 0.20 mass-%, or at least 0.11 mass-% Vanadium, or at least 0.12 mass-% Vanadium, or at least 0.13 mass-% Vanadium, or at least 0.14 mass-% Vanadium in order to assure high strength. It has however been found that a too high amount of Vanadium is detrimental to the impact toughness of the quenched and tempered steel. The amount of Vanadium should not therefore exceed 0.25 mass-%. Vanadium has a strong precipitation strengthening effect after tempering and is needed to achieve high strength both in base metal and in the HAZ.
- Aluminium is used to condense steel, i.e. to bind oxygen from the steel. The Aluminium content is 0.01 - 0.15 mass-%, preferably 0.015 - 0.08 mass-% to prevent excessive formation of aluminium oxides.
- Boron is an effective alloying element that promotes hardenability of the steel in quenching. It is an essential alloying element in this invention since it promotes strength and hardness properties in the weld metal and heat-affected zone (HAZ). During welding, Boron moves from the base material to the weld metal, thereby increasing the hardness of the weld metal. This ensures that fracture does not occur in the weld metal or fusion line. Fracture can be moved as far as possible away from the fusion line towards the base material in high static loads. The Boron content is 0.0005 - 0.010 mass-%, preferably 0.0005 - 0.005 mass-% and more preferably 0.001 - 0.003 mass-%. A Boron content of at least 0.0005 mass-% promotes hardenability of the base material and of the HAZ, ensuring good strength properties. On the other hand, a Boron content of more than 0.005 mass-% is worthless as regards the hardenability of the base material and the HAZ. When the Boron content is more than 0.001 mass-%, it ensures matching strength properties of the weld and fracture location as previously described. A Boron content of more than 0.010 mass-% can be detrimental for mechanical properties of the steel.
- The Chromium content of hot-rolled steel according to the present invention is 0. 1 - 1.7 mass-%, preferably 0.4 - 1.7 or 0.6 - 1.5 mass-%, or more than 1.0 mass-% in order to achieve high strength and good hardenability both in the hot-rolled steel as produced and in the HAZ of a welded hot-rolled steel product. Chromium also promotes tempering resistance.
- According to an embodiment of the invention the chemical composition of hot-rolled steel according to the present invention contains both Ni and Cu in a total amount of at least 0.5 mass-%, or at least 1.0 mass-%, or at least 1.2 mass-%. Copper is an optional alloying element. It can be used in an amount up to 1.5 mass-%, preferably 0.1-1.0 mass-% in order to increase the strength or improve the weather resistance of the hot-rolled steel.
- According to an embodiment of the invention the chemical composition contains both Ni and Cu, and the amount of Ni ≥ 0.33 x the amount of Cu, preferably the amount of Ni ≥ 0.5 x the amount of Cu. Cr+Cu+Ni is between 0.4 - 5.7, preferably between 1.4 - 3.5 and more preferably between 2 - 3.
- Nickel is an essential alloying element in the hot-rolled steel according to the present invention and it improves the toughness of the heat-affected zones and the weld metal of welded seams and it also improves the surface quality of the hot-rolled steel containing Copper but may, under some circumstances, slightly decrease the impact toughness of the tempered steel.
- Phosphorus weakens the impact toughness of quenched and tempered steel and the Phosphorus content should therefore be limited to a maximum of 0.015 mass-%, preferably to a maximum of 0 - 0.009 mass-%.
- Sulphur content is limited to a maximum of 0.008 mass-%, preferably to a maximum of 0.004 mass-%, to assure good impact toughness and formability in the hot-rolled steel according to the present invention.
- Zirconium is an optional alloying element that may replace Niobium if needed. The Zirconium content can be between 0 - 0.2 mass-%, preferably 0 - 0.01 mass-%.
- Calcium is an optional alloying element that may be used to modify the morphology of inclusions in the steel. The Calcium content can be between 0 - 0.004 mass-%. If the amount of Calcium exceeds 0.004 mass-% the inclusions in the steel may be too large, which may adversely affect the physical properties of the steel.
- The hot-rolled steel has a tensile strength of at least 1120 MPa and up to 1450 MPa.
- According to an embodiment of the invention the hot-rolled steel has an A%-elongation of at least 8% (i.e. permanent elongation of length, expressed in percent of length) or even of at least 10% or at least 12% along and transverse to the rolling direction. The hot-rolled steel has such an elongation in its as-produced condition. The hot-rolled steel also has an elongation of at least 7%, preferably at least 8%, more preferably at least 9% when a tensile test is carried out across a weld seam of a welded hot-rolled steel product where the weld is longitudinal to the rolling direction.
- According to an embodiment of the invention the hot-rolled steel an impact toughness of at least 34 J/cm2 and more preferably an impact toughness of at least 50 J/cm2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -20°C and more preferably at -40°C longitudinally and transverse to the rolling direction. The hot-rolled steel has such an impact strength in its as-produced condition.
- The mechanical properties of the hot-rolled steel cited in this document were determined in accordance with the testing instructions of standard ISO 10025-6:2004.
- According to an embodiment of the invention the hot-rolled steel is metal active gas (MAG) welded with our without reinforcement, using a V- or Y-groove welding method, whereby a first pass is welded from a bottom or top side, preferably from a bottom side, and other passes from a top side, using welding consumables having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds, which may be determined by welding the hot-rolled steel and measuring the time it takes for the weld seam and the adjacent heat-affected zone (HAZ) to cool from 800°C to 500°C.
- According to an embodiment of the invention the hot-rolled steel has a minimum bending radius of 5.0 x thickness or more preferably a minimum bending radius of 4.0 x thickness or more preferably a minimum bending radius of 3.5 x thickness longitudinally and transverse to the rolling direction. With a plate thickness of 7 mm or more the steel has a minimum bending radius of 5.0 x thickness or preferably a minimum bending radius of 4.0 x thickness or more preferably a minimum bending radius of 3.5 x thickness longitudinally to the rolling direction, and a minimum bending radius of 5.0 x thickness transverse to the rolling direction.
- The hot-rolled steel according to the present invention is suitable for applications, such as wear or structural applications, in which the steel must exhibit high strength in combination with sufficient hardness, bendability and impact toughness both in the as-produced products and in the HAZ (heat affected zone) of welded hot-rolled steel products. For example, the hot-rolled steel according to the present invention may be used to produce any component for construction, mining, material-handling, earth-moving, pile driving, snow-plowing, landscaping or rock drilling equipment. The hot-rolled steel may for example be used to produce a lifting boom for an excavator or crane.
- Tests were conducted using the steels having the chemical compositions presented in Table 1 below. The amount of each element is given in mass-%, the balance being Fe and unavoidable impurities other than Nitrogen. It should be noted that Nitrogen may also be considered to be an unavoidable impurity. The amount of Nitrogen is however given in Table 1 along with the intentionally added alloying elements. The amount of Nitrogen is in the range of 0-0.01 mass-%.
- It should be noted that the compositions labelled "INV" in Table 1 are steels that have the chemical composition and the physical properties of steel according to the present invention and which have been manufactured using a method according to the present invention. Comparative examples that do not have the chemical composition or the physical properties of steel according to the present invention, or which have not been manufactured using a method according to the present invention are labelled "REF" in Table 1.
Table 1: Chemical compositions Comp. C Si Mn P S Al Nb V Cu Cr Ni N Mo Ti Ca B INV/ REF A1 0.13 0.20 1.5 0.01 0.001 0.05 0.00 0.15 0.4 1.3 1.0 0.004 0.4 0.01 0.002 0.001 INV B 0.14 0.18 1.5 0.01 0.001 0.05 0.00 0.15 0.5 1.3 2.0 0.004 0.1 0.01 0.002 0.001 REF C 0.17 0.19 1.5 0.01 0.001 0.05 0.04 0.05 0.5 0.7 1.0 0.004 0.4 0.01 0.002 0.001 INV A2 0.13 0.20 1.5 0.01 0.002 0.05 0.00 0.15 0.5 1.4 1.0 0.004 0.4 0.01 0.003 0.002 INV A3 0.13 0.18 1.5 0.01 0.002 0.06 0.00 0.15 0.4 1.3 1.0 0.004 0.4 0.01 0.003 0.001 INV D 0.17 0.30 1.5 0.01 0.001 0.05 0.00 0.04 0.4 0.7 1.0 0.003 0.4 0.02 0.001 0.000 REF E 0.13 0.19 1.5 0.01 0.001 0.05 0.00 0.04 0.4 0.7 1.5 0.003 0.4 0.02 0.001 0.000 REF F 0.17 0.19 1.5 0.01 0.001 0.06 0.00 0.04 0.4 0.7 1.0 0.003 0.4 0.02 0.001 0.001 REF G 0.18 0.03 1.5 0.01 0.001 0.05 0.00 0.04 0.4 1.0 1.0 0.003 0.4 0.02 0.001 0.001 REF - Steels having the chemical compositions presented in Table 1 were hot-rolled to an end thickness of 4 mm, 6 mm and 8 mm. Hot-rolling was performed in a hot strip rolling line and hot-rolled strips were directly quenched after rolling before coiling. Depending on the type of tempering furnace used, the tempering was carried out before or after a cut-to-length process. If the tempering was performed in bell type furnace (tempering code "C" in Table 2 below), then the cut-to-length processing for quenched strips was carried out after tempering. In the case of sheet tempering (tempering code "S" in Table 2), the cut-to-length processing was carried out before the tempering annealing. Depending on the tempering method, the holding time during tempering varied between 15 - 720 minutes.
- More specific manufacturing parameters are presented in Table 2.
Table 2: Process parameters composition process tempering thickness furnT FRT CT T t I NV/REF code code code mm °C °C °C °C min A1 R02 S600 8.0 1280 856 50 600 30 INV B R04 S600 8.0 1280 862 50 600 30 REF c R06 S560 8.0 1280 878 50 560 30 INV A2 R12 S600 4.0 1278 924 50 600 15 INV A2 R13 S585 8.0 1267 871 50 585 15 INV A2 R13 S600 8.0 1267 871 50 600 15 INV A3 R14 S585 6.0 1279 897 50 585 15 INV A3 R14 S600 6.0 1279 897 50 600 15 INV A2 R16 S585 4.0 1279 917 50 585 15 INV A2 R16 S600 4.0 1279 917 50 600 15 INV D B05 C420 6.0 1250 919 100 420 720 REF A1 B09 C200 8.0 1250 891 100 200 720 REF E B10 C600 6.0 1250 876 100 600 240 REF F B12 C450 6.0 1250 897 100 450 540 REF G B14 C450 6.0 1250 918 100 450 540 REF D B15 C600 6.0 1250 917 100 600 240 REF - where: furnT = reheat temperature before hot-rolling
- FRT = finishing rolling temperature
- CT = coiling temperature
- T = tempering temperature
- t = tempering time
- Test results from mechanical tests and bending tests are presented in Table 3. Steels according to invention have a mechanical properties as stipulated in claim 1.
- Bending tests were carried out using three-point bending with samples having an area of 300 x 300 mm2. Samples were bent to an angle of 90° with one press and all samples were bent into a Z-shape so that both the upper and lower surfaces of the samples were tested. Mechanical properties and bendability of the samples were tested both longitudinally with respect to the rolling direction, and transversely with respect to the rolling direction.
Table 3: Physical properties composition code rolling code tempering code thickness mm test direction T/L Rp0.2 MPa Rm MPa A% % T_test °C CV J CV J/cm2 Bendability INV/REF Ri/t A1 R02 S600 8.0 T 1151 1188 13.6 -40 33 55.0 4.5 INV A1 R02 S600 8.0 L 1170 1180 15.0 -40 46 76.7 2.8 INV B R04 S600 8.0 T 1096 1128 14.7 -40 28 46.7 4.0 REF B R04 S600 8.0 L 1108 1119 15.4 -40 35 58.3 2.8 REF C R06 S560 8.0 T 1158 1196 13.3 -40 23 38.3 3.5 INV C R06 S560 8.0 L 1171 1185 14.2 -40 42 70.0 2.8 INV A2 R12 S600 4.0 T 1111 1166 13.9 -40 10 50.0 2.0 INV A2 R12 S600 4.0 L 1117 1170 15.1 -40 15 75.0 2.3 INV A2 R13 S585 8.0 T 1170 1204 14.0 -40 29 48.3 2.1 INV A2 R13 S585 8.0 L 1155 1177 15.1 -40 46 76.7 2.8 INV A2 R13 S600 8.0 T 1163 1196 14.0 -40 28 46.7 2.1 INV A2 R13 S600 8.0 L 1151 1171 15.4 -40 47 78.3 2.5 INV A3 R14 S585 6.0 T 1129 1173 14.5 -40 18 45.0 2.3 INV A3 R14 S585 6.0 L 1118 1152 15.6 -40 30 75.0 2.7 INV A3 R14 S600 6.0 T 1128 1171 14.2 -40 18 45.0 2.2 INV A3 R14 S600 6.0 L 1115 1147 15.5 -40 32 80.0 2.3 INV A2 R16 S585 4.0 T 1134 1178 14.6 -40 16 50.0 2.0 INV A2 R16 S585 4.0 L 1134 1163 15.8 -40 24 75.0 2.8 INV D B05 C420 6.0 T 1182 1277 7.3 -40 17 42.5 3.2 REF D B05 C420 6.0 L 1125 1251 9.0 -40 21 52.5 3.2 REF A1 B09 C200 8.0 T 1349 1551 6.7 -40 53 88.3 2.5 REF A1 B09 C200 8.0 L 1327 1519 9.0 -40 79 131.7 3.4 REF E B10 C600 6.0 T 1098 1137 8.9 -40 27 67.5 2.2 REF E B10 C600 6.0 L 1023 1108 11.8 -40 35 87.5 2.3 REF F B12 C450 6.0 T 1170 1257 7.9 -40 20 50.0 2.8 REF F B12 C450 6.0 L 1098 1229 8.9 -40 29 72.5 3.3 REF G B14 C450 6.0 T 1180 1265 7.0 -40 19 47.5 2.7 REF G B14 C450 6.0 L 1105 1234 9.9 -40 28 70.0 3.2 REF D B15 C600 6.0 T 1095 1143 8.7 -40 19 47.5 1.8 REF D B15 C600 6.0 L 1028 1132 11.3 -40 30 75.0 2.0 REF - Welding tests were carried out using a metal active gas (MAG) welding method and V- and Y -grooves. The welding consumables used were according to standard ENG 89 5 M21 Mn4Ni2.5CrMo (Commercial grade X96). The first pass was welded from bottom or top side, preferably from the bottom side, and others passes were welded from the top side. Welding consumables having a tensile strength of 960 MPa were used and t8/5 was varied between 6 - 18 seconds. Tensile tests across the weld showed that the weld had a yield strength of 1100 MPa (Rp0.2) and the fracture was located at the base metal (BM).
- The target was to achieve a combination of strength and toughness properties which are as good as possible in the weld so that matching tensile properties can be achieved without losing toughness. In addition, the aim was to obtain a fracture in a static tensile test over the weld that is located as far as possible from the weld metal (WM) and fusion line (FL), which enables extremely good elongation to fracture values for the welded structure. The behaviour of a welded structure is predictable and safe when the fracture in static loading takes place as far as possible away from the WM and FL and the elongation to fracture is high. The inventors have found that steels according to the present invention can fulfill these requirements even if the yield strength for the base material is more than 1100 MPa. Usually, known steels with such a high strength have a fracture located over the weld (WM or FL) when a tensile test is performed, especially when un-matching welding consumables are used (the yield strength of un-matching welding consumables is typically less than 1100 MPa).
- Table 4 shows the welding parameters that were used in the tests and the test results obtained. Steels according the invention have a fracture that is located at a distance from the weld (WM and/or FL) when a static load in a tensile test is set over the weld. It is surprising compared to known steels that such behaviour can be achieved with or even without reinforcement. Without reinforcement, the achievement of such behaviour is very innovative. Fracture location is labelled "BM" in Table 4 when the fracture is in the base material, "HAZ" when it occurs in the Heat Affected Zone, and "WM" when the fracture occurs in the Weld Metal.
Table 4: Welding results Processing variables Transverse tensile test on weld Cha rpy V (5x10x55 mm) INV/REF Without reinforcement With reinforcement J /-40°C (mea n of 3 tests) composition code rolling code tempering code thickness mm t8/5s Rp0.2 MPa Rm MPa A%% fracture location Rp0.2 MPa Rm MPa A%% fracture location WM FL FL+1 FL+3 FL+5 A1 R02 S600 8 12 1125 1201 11,8 BM 1140 1194 10,8 BM 18 ≠ 25 37 20 INV B R04 S600 8 12 1078 1130 11,2 BM 1080 1123 11,2 BM 16 19 31 33 19 REF C R05 S560 8 6 1154 1213 9,8 BM 1160 1204 9,6 BM ≠ 18 31 18 17 INV C R05 S560 8 12 1140 1212 10,0 BM 1143 1201 10,3 BM 20 18 24 32 18 INV C R05 S560 8 18 1115 1207 10,5 BM 1135 1198 10,4 BM 22 19 26 34 15 INV D B05 C420 6 6 1128 1233 4,7 HAZ 1174 1275 8,4 BM 27 27 36 24 25 REF D B05 C420 6 12 1081 1185 4,0 WM 1157 1252 6,2 HAZ 31 33 49 32 28 REF D B05 C420 6 18 1067 1175 5,0 WM 1162 1248 5,5 HAZ 35 43 53 35 30 REF F B12 C450 6 12 1101 1208 5,1 WM 1162 1244 7,3 HAZ 31 30 33 53 28 REF G B14 C450 6 12 1106 1217 5,2 WM 1161 1247 5,7 HAZ 27 29 32 40 26 REF A2 R12 S600 4 12 1107 1176 11,7 BM 1118 1190 11,6 BM ≠ ≠ ≠ ≠ ≠ INV
Impact toughness was measured using specimens having a thickness of 5 mm. -
Figures 2 and3 shows typical hardness profiles over the welded seam tested near the face side and the root side of the welded samples. It is surprising that steels according to the present invention can have a very smooth hardness profile over the weld and that there are no soft zones that could start to neck during a tensile test and thereby influence the location of the fracture. Normally, steels with a yield strength of 1100 MPa welded with un-matching welding consumables (X90 and/or X96) exhibit some softening in the HAZ and especially in the WM. Steel according to the invention can maintain good hardness in the HAZ but also have good hardness in the WM due to the diffusion of alloying elements promoting hardening (i.e. Boron). Low carbon content in the steels according to the invention (i.e. 0.1 - 0.20 mass-% Carbon) ensures that a weld has high toughness as well as good hardness. - Further modifications of the invention within the scope of the claims would be apparent to a skilled person.
Claims (13)
- Hot-rolled steel having a yield strength Rp0.2 of at least 1100 MPa along and transverse to a rolling direction and a tensile strength of at least 1120 MPa and up to 1450 MPa along and transverse to a rolling direction, characterized in that: it has an A%-elongation of at least 8% along and/or transverse to the rolling direction, an impact toughness of at least 34 J/cm2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -40°C longitudinally to the rolling direction, a minimum bending radius of 5.0 x thickness longitudinally and/or transverse to the rolling direction, and a chemical composition containing in mass-%:• C 0.10 - 0.2• Si 0 - 0.7• Mn 1.3 - 2.2• Nb 0 - 0.06• Ti 0 - 0.15• V more than 0.03 and ≤ 0.25• Al 0.01 - 0.15• B 0.0005 - 0.010• Cr 0.1 - 1.7• Mo 0.15 - 0.8• Cu 0 - 1.5• Ni 0.3 - 2.5• P 0 - 0.015• S 0 -0.008• Zr 0 - 0.2• Ca 0 - 0.004• N 0-0.01• balance Fe and unavoidable impurities,whereby:a) when 0.10 < C < 0.11 then Mn ≥ 1.60 and V > 0.14 and Mo ≥ 0.5b) when 0.11 ≤ C < 0.125 then Mn ≥ 1.45 and V ≥ 0.13 and Mo ≥ 0.35c) when 0.125 ≤ C < 0.15, then Mn ≥ 1.35 and V ≥ 0.12 and Mo ≥ 0.20, andd) when C ≥ 0.15 and V > 0.11, then Mn ≥ 1.3 and Mo ≥ 0.15 orwhen C ≥ 0.15 and V 0.03 - 0.11, then Mn > 1.3 and Mo > 0.15 and Nb > 0.02 and Cr+Cu+Ni >1.4.
- Hot-rolled steel according to claim 1, whereby said chemical composition comprises 0.4-1.7 mass-% Cr, preferably 1.0 -1.7 mass-% Cr.
- Hot-rolled steel according to claim 1 or 2, whereby said chemical composition contains both Ni and Cu, in a total amount of at least 0.5 mass-%, preferably at least 1 mass-%.
- Hot-rolled steel according to any of the preceding claims, whereby the steel has an A%- elongation of at least 10% or more preferably at least 12% along and/or transverse to the rolling direction.
- Hot-rolled steel according to any of the preceding claims, whereby the steel has an impact toughness of at least 50 J/cm2 when a Charpy V notched specimen having a thickness of 5-10 mm is measured at -40°C longitudinally to the rolling direction.
- Hot-rolled steel according to any of the preceding claims, whereby the steel has a minimum bending radius of 4.0 x thickness longitudinally and/or transverse to the rolling direction, more preferably a minimum bending radius of 3.5 x thickness longitudinally.
- Hot-rolled steel according to any of the preceding claims, whereby the steel has an A%- elongation of at least 7%, preferably of at least 8% or more preferably at least 9% when a tensile test is carried out across a weld seam of a welded hot-rolled steel product where the weld is longitudinal to the rolling direction, whereby said hot-rolled steel is welded using metal active gas (MAG) welding with reinforcement, using a V- or Y-groove welding method, whereby a first pass is welded from a bottom or top side, preferably from a bottom side, and other passes from a top side, using welding consumables according to standard ENG 89 5 M21, commercial grade(s) X90 and/or X96, having a tensile strength of 890 MPa, preferably 960 MPa, more preferably 1100 MPa and a t8/5 of 5 - 20 seconds, preferably 6 - 18 seconds, or 8-12 seconds, whereby the welded steel has a fracture that is located at a distance of at least 1 mm from the fusion line.
- Method for manufacturing hot-rolled steel according to claim 1, whereby the method comprises the following steps:- heating a steel slab having a chemical composition according to claim 1 to an austenitizing temperature of 1000 - 1350 °C,- hot-rolling such that a finishing rolling temperature is 760 - 1050°C,- quenching to a temperature of 300 °C or less, and temper annealing at a temperature of 500 - 650 °C if the tempering time is 1 hour or more, or temper annealing at a temperature of 500 - 750 °C if the tempering time is less than 1 hour after said quenching step, whereby the microstructure of the hot-rolled steel before the temper annealing step contains at least 90 area-% martensite when said microstructure is examined in ¼ thickness, and the content of ferrite and pearlite before the temper annealing step must be in total less than 10 area-%.
- Method according to claim 8, whereby the microstructure of the hot-rolled steel before said temper annealing step contains at least 95 area-% martensite and more preferably at least 99 area-% martensite when said microstructure is examined in ¼ thickness.
- Method according to claim 8 or 9, whereby said quenching step is a direct quenching step.
- Method according to any of claims 8-10, whereby the method comprises the step of strip rolling said hot-rolled steel and said hot-rolled steel comprises a maximum of 0.005 mass-% Niobium and < 0.15 mass-% Carbon.
- Method according to any of claims 8-10, whereby said hot-rolled steel comprises a minimum of 0.005 mass-% Niobium, preferably a minimum of 0.02 mass-% Niobium when the hot-rolled steel is not strip rolled.
- Use of a hot-rolled steel according to any of claims 1-7 for metal active gas (MAG) welding with reinforcement, using a V- or Y-groove welding method, whereby a first pass is welded from a bottom or top side, preferably from a bottom side, and other passes from a top side, using welding consumables according to standard ENG 89 5 M21, commercial grade(s) X90 and/or X96, having a tensile strength of 1100 MPa, preferably 960 MPa, more preferably 900 MPa, most preferably 890 MPa, and a t8/5 time of 8 - 12 seconds, preferably 6 - 18 seconds, more preferably 5-20 seconds, wherein the t8/5 time is the time it takes for the total weld area to cool from 800°C to 500°C , whereby the welded steel has a fracture that is located at a distance of at least 1 mm from the fusion line.
Priority Applications (9)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| HUE18152884A HUE052103T2 (en) | 2018-01-23 | 2018-01-23 | Hot rolled steel and process for the production of hot rolled steel |
| ES18152884T ES2835285T3 (en) | 2018-01-23 | 2018-01-23 | Hot rolled steel and method of making hot rolled steel |
| EP18152884.5A EP3514253B1 (en) | 2018-01-23 | 2018-01-23 | Hot-rolled steel & method for manufacturing hot-rolled steel |
| BR112020014887-3A BR112020014887B1 (en) | 2018-01-23 | 2019-01-16 | HOT ROLLED STEEL & METHOD FOR MANUFACTURING HOT ROLLED STEEL |
| KR1020207023837A KR20200109361A (en) | 2018-01-23 | 2019-01-16 | Hot-rolled steel & method for manufacturing hot-rolled steel |
| PCT/EP2019/051006 WO2019145196A1 (en) | 2018-01-23 | 2019-01-16 | Hot-rolled steel & method for manufacturing hot-rolled steel |
| JP2020560553A JP2021511441A (en) | 2018-01-23 | 2019-01-16 | Hot-rolled steel and hot-rolled steel manufacturing method |
| CN201980009512.5A CN111630200B (en) | 2018-01-23 | 2019-01-16 | Hot-rolled steel and method for producing hot-rolled steel |
| US16/961,724 US20230203609A1 (en) | 2018-01-23 | 2019-01-16 | Hot-rolled steel & method for manufacturing hot-rolled steel |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP18152884.5A EP3514253B1 (en) | 2018-01-23 | 2018-01-23 | Hot-rolled steel & method for manufacturing hot-rolled steel |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3514253A1 EP3514253A1 (en) | 2019-07-24 |
| EP3514253B1 true EP3514253B1 (en) | 2020-10-14 |
Family
ID=61131953
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP18152884.5A Active EP3514253B1 (en) | 2018-01-23 | 2018-01-23 | Hot-rolled steel & method for manufacturing hot-rolled steel |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US20230203609A1 (en) |
| EP (1) | EP3514253B1 (en) |
| JP (1) | JP2021511441A (en) |
| KR (1) | KR20200109361A (en) |
| CN (1) | CN111630200B (en) |
| ES (1) | ES2835285T3 (en) |
| HU (1) | HUE052103T2 (en) |
| WO (1) | WO2019145196A1 (en) |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA3095046A1 (en) | 2018-03-29 | 2019-10-03 | Oerlikon Metco (Us) Inc. | Reduced carbides ferrous alloys |
| EP3870727A1 (en) | 2018-10-26 | 2021-09-01 | Oerlikon Metco (US) Inc. | Corrosion and wear resistant nickel based alloys |
| CN113631750A (en) | 2019-03-28 | 2021-11-09 | 欧瑞康美科(美国)公司 | Thermally sprayed iron-based alloys for coating engine cylinder bores |
| CA3136967A1 (en) | 2019-05-03 | 2020-11-12 | Oerlikon Metco (Us) Inc. | Powder feedstock for wear resistant bulk welding configured to optimize manufacturability |
| KR102870036B1 (en) | 2019-07-09 | 2025-10-13 | 오를리콘 메트코 (유에스) 아이엔씨. | Iron-based alloys designed for wear and corrosion resistance |
| CN112233735B (en) * | 2020-09-07 | 2022-04-19 | 包头钢铁(集团)有限责任公司 | Design method for chemical components of pearlitic rail steel |
| CN113528974B (en) * | 2021-06-18 | 2022-06-21 | 首钢集团有限公司 | Steel for protection and preparation method thereof |
| CN117089760A (en) * | 2022-05-11 | 2023-11-21 | 宝山钢铁股份有限公司 | A kind of high fatigue performance steel for rock drilling tools and its manufacturing method |
| CN116219279B (en) * | 2022-12-23 | 2024-04-16 | 鞍钢股份有限公司 | A high-strength and high-toughness steel for nuclear reactor containment and a manufacturing method thereof |
| CN118745547A (en) * | 2024-06-12 | 2024-10-08 | 无锡市华尔泰机械制造有限公司 | A method for manufacturing high-strength corrosion-resistant steel forged pipe fittings |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4696570B2 (en) * | 2005-01-26 | 2011-06-08 | Jfeスチール株式会社 | Manufacturing method of high-tensile steel material with excellent hydrogen embrittlement resistance |
| JP5277648B2 (en) * | 2007-01-31 | 2013-08-28 | Jfeスチール株式会社 | High strength steel sheet with excellent delayed fracture resistance and method for producing the same |
| JP4410836B2 (en) * | 2008-04-09 | 2010-02-03 | 新日本製鐵株式会社 | Method for producing 780 MPa class high strength steel sheet having excellent low temperature toughness |
| CN101835918B (en) * | 2008-09-17 | 2011-12-21 | 新日本制铁株式会社 | High-strength thick steel plate and manufacturing method thereof |
| JP5604849B2 (en) * | 2009-10-22 | 2014-10-15 | Jfeスチール株式会社 | High-tensile thick steel plate with excellent hydrogen penetration inhibition characteristics and method for producing the same |
| FI122313B (en) * | 2010-06-07 | 2011-11-30 | Rautaruukki Oyj | Process for the production of hot rolled steel product and hot rolled steel |
| WO2013099192A1 (en) * | 2011-12-27 | 2013-07-04 | Jfeスチール株式会社 | High-tension hot rolled steel sheet and method for manufacturing same |
| JP5838796B2 (en) * | 2011-12-27 | 2016-01-06 | Jfeスチール株式会社 | High-strength hot-rolled steel sheet excellent in stretch flangeability and manufacturing method thereof |
| CN103060715B (en) * | 2013-01-22 | 2015-08-26 | 宝山钢铁股份有限公司 | A kind of ultra-high strength and toughness steel plate and manufacture method thereof with low yielding ratio |
-
2018
- 2018-01-23 EP EP18152884.5A patent/EP3514253B1/en active Active
- 2018-01-23 HU HUE18152884A patent/HUE052103T2/en unknown
- 2018-01-23 ES ES18152884T patent/ES2835285T3/en active Active
-
2019
- 2019-01-16 JP JP2020560553A patent/JP2021511441A/en not_active Withdrawn
- 2019-01-16 KR KR1020207023837A patent/KR20200109361A/en not_active Withdrawn
- 2019-01-16 CN CN201980009512.5A patent/CN111630200B/en active Active
- 2019-01-16 WO PCT/EP2019/051006 patent/WO2019145196A1/en not_active Ceased
- 2019-01-16 US US16/961,724 patent/US20230203609A1/en not_active Abandoned
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2019145196A1 (en) | 2019-08-01 |
| JP2021511441A (en) | 2021-05-06 |
| KR20200109361A (en) | 2020-09-22 |
| US20230203609A1 (en) | 2023-06-29 |
| CN111630200B (en) | 2022-07-05 |
| BR112020014887A2 (en) | 2020-12-08 |
| EP3514253A1 (en) | 2019-07-24 |
| CN111630200A (en) | 2020-09-04 |
| HUE052103T2 (en) | 2021-04-28 |
| ES2835285T3 (en) | 2021-06-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20230203609A1 (en) | Hot-rolled steel & method for manufacturing hot-rolled steel | |
| KR102276741B1 (en) | High strength cold-rolled steel sheet and galvanized steel sheet having high hole expansion ratio and manufacturing method thereof | |
| US12522888B2 (en) | Method of manufacutring a high-strength cold rolled steel sheet having high hole expansion ratio, and highstrength hot-dip galvanized steel sheet | |
| KR102412400B1 (en) | Cold rolled steel sheet having excellent spot weldability, strength and formability and method of manufacturing the same | |
| EP3653736B1 (en) | Hot-rolled steel strip and manufacturing method | |
| EP2576848B1 (en) | Method for producing a hot-rolled steel product, and a hot-rolled steel | |
| US10604817B2 (en) | High-strength steel plate for pressure vessel having excellent toughness after post weld heat treatment and manufacturing method thereof | |
| JP4975888B2 (en) | Ni-added steel sheet and manufacturing method thereof | |
| RU2586953C2 (en) | Heavy-duty structural steel and manufacturing method thereof | |
| EP2520680B1 (en) | High strength steel sheet having excellent resistance to post weld heat treatment and method for manufacturing same | |
| EP2592168B1 (en) | Abrasion resistant steel plate with excellent impact properties and method for producing said steel plate | |
| KR101736632B1 (en) | Cold-rolled steel sheet and galvanized steel sheet having high yield strength and ductility and method for manufacturing thereof | |
| JP2001164338A (en) | Automotive high strength electric resistance welded tube excellent in delayed fracture resistance and producing method therefor | |
| JP2008266758A (en) | High tensile steel with excellent low temperature toughness and low strength anisotropy and method for producing the same | |
| JP2009242841A (en) | High-tensile steel excellent in bending workability and low-temperature toughness, and method for manufacturing the same | |
| JP6691967B2 (en) | High hardness and wear resistant steel excellent in toughness and cutting crack resistance, and method for producing the same | |
| CA3094517C (en) | A steel composition in accordance with api 5l psl-2 specification for x-65 grade having enhanced hydrogen induced cracking (hic) resistance, and method of manufacturing the steel thereof | |
| KR102321269B1 (en) | High strength steel sheet and manufacturing method thereof | |
| JP4696570B2 (en) | Manufacturing method of high-tensile steel material with excellent hydrogen embrittlement resistance | |
| KR102544854B1 (en) | Cold rolled annealed steel sheet with high hole expansion ratio and manufacturing process thereof | |
| KR101999000B1 (en) | High-manganese steel sheet having excellent welding strength and method for manufacturing thereof | |
| KR101304852B1 (en) | Steel sheet having excellent weldability, hardness uniformity in the thickness direction and low temperature toughness, and method for manufacturing the same | |
| JP2022510209A (en) | Medium- and high-temperature steel sheets with excellent high-temperature strength and their manufacturing methods | |
| KR20150001469A (en) | High strength cold-rolled steel sheet and method of manufacturing the cold-rolled steel sheet | |
| KR101696051B1 (en) | Steel sheet having excellent resistance and excellent low temperature toughness to hydrogen induced cracking, and method of manufacturing the same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17P | Request for examination filed |
Effective date: 20190426 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17Q | First examination report despatched |
Effective date: 20190709 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C22C 38/50 20060101ALI20200316BHEP Ipc: C22C 38/02 20060101ALI20200316BHEP Ipc: C22C 38/48 20060101ALI20200316BHEP Ipc: C22C 38/42 20060101ALI20200316BHEP Ipc: C21D 6/00 20060101ALI20200316BHEP Ipc: C22C 38/44 20060101ALI20200316BHEP Ipc: C22C 38/06 20060101ALI20200316BHEP Ipc: C21D 1/20 20060101ALI20200316BHEP Ipc: C22C 38/54 20060101ALI20200316BHEP Ipc: C22C 38/00 20060101AFI20200316BHEP Ipc: C22C 38/04 20060101ALI20200316BHEP Ipc: C21D 1/25 20060101ALI20200316BHEP Ipc: C22C 38/46 20060101ALI20200316BHEP Ipc: C21D 8/02 20060101ALI20200316BHEP Ipc: C21D 1/18 20060101ALI20200316BHEP Ipc: C21D 8/04 20060101ALI20200316BHEP Ipc: C21D 9/46 20060101ALI20200316BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20200401 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C21D 6/00 20060101ALI20200320BHEP Ipc: C21D 1/20 20060101ALI20200320BHEP Ipc: C21D 1/25 20060101ALI20200320BHEP Ipc: C22C 38/44 20060101ALI20200320BHEP Ipc: C22C 38/48 20060101ALI20200320BHEP Ipc: C21D 8/04 20060101ALI20200320BHEP Ipc: C21D 9/46 20060101ALI20200320BHEP Ipc: C21D 8/02 20060101ALI20200320BHEP Ipc: C22C 38/06 20060101ALI20200320BHEP Ipc: C22C 38/42 20060101ALI20200320BHEP Ipc: C22C 38/46 20060101ALI20200320BHEP Ipc: C21D 1/18 20060101ALN20200320BHEP Ipc: C22C 38/50 20060101ALI20200320BHEP Ipc: C22C 38/04 20060101ALI20200320BHEP Ipc: C22C 38/54 20060101ALI20200320BHEP Ipc: C22C 38/02 20060101ALI20200320BHEP Ipc: C22C 38/00 20060101AFI20200320BHEP |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| GRAL | Information related to payment of fee for publishing/printing deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR3 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| INTC | Intention to grant announced (deleted) | ||
| GRAR | Information related to intention to grant a patent recorded |
Free format text: ORIGINAL CODE: EPIDOSNIGR71 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C22C 38/48 20060101ALI20200820BHEP Ipc: C21D 9/46 20060101ALI20200820BHEP Ipc: C21D 6/00 20060101ALI20200820BHEP Ipc: C22C 38/02 20060101ALI20200820BHEP Ipc: C22C 38/04 20060101ALI20200820BHEP Ipc: C22C 38/00 20060101AFI20200820BHEP Ipc: C22C 38/54 20060101ALI20200820BHEP Ipc: C22C 38/46 20060101ALI20200820BHEP Ipc: C21D 8/04 20060101ALI20200820BHEP Ipc: C22C 38/50 20060101ALI20200820BHEP Ipc: C21D 8/02 20060101ALI20200820BHEP Ipc: C22C 38/06 20060101ALI20200820BHEP Ipc: C22C 38/42 20060101ALI20200820BHEP Ipc: C22C 38/44 20060101ALI20200820BHEP Ipc: C21D 1/20 20060101ALI20200820BHEP Ipc: C21D 1/25 20060101ALI20200820BHEP Ipc: C21D 1/18 20060101ALN20200820BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20200902 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1323635 Country of ref document: AT Kind code of ref document: T Effective date: 20201015 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602018008582 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: FGE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E052103 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210215 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210114 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210115 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210214 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210114 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2835285 Country of ref document: ES Kind code of ref document: T3 Effective date: 20210622 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602018008582 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| 26N | No opposition filed |
Effective date: 20210715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210123 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210131 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210123 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210214 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 1323635 Country of ref document: AT Kind code of ref document: T Effective date: 20201014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201014 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250416 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251222 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20251223 Year of fee payment: 9 Ref country code: FR Payment date: 20251224 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20251223 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20251222 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20251212 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20251222 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251211 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260116 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20260128 Year of fee payment: 9 Ref country code: FI Payment date: 20260217 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20260122 Year of fee payment: 9 |