EP2314517B1 - Method for reinforcing a post of a shipping pallet - Google Patents
Method for reinforcing a post of a shipping pallet Download PDFInfo
- Publication number
- EP2314517B1 EP2314517B1 EP10013968A EP10013968A EP2314517B1 EP 2314517 B1 EP2314517 B1 EP 2314517B1 EP 10013968 A EP10013968 A EP 10013968A EP 10013968 A EP10013968 A EP 10013968A EP 2314517 B1 EP2314517 B1 EP 2314517B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- post
- providing
- posts
- wall
- reinforcing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P11/00—Connecting or disconnecting metal parts or objects by metal-working techniques not otherwise provided for
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D19/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D19/0004—Rigid pallets without side walls
- B65D19/0006—Rigid pallets without side walls the load supporting surface being made of a single element
- B65D19/0008—Rigid pallets without side walls the load supporting surface being made of a single element forming a continuous plane contact surface
- B65D19/001—Rigid pallets without side walls the load supporting surface being made of a single element forming a continuous plane contact surface the base surface being made of a single element
- B65D19/0014—Rigid pallets without side walls the load supporting surface being made of a single element forming a continuous plane contact surface the base surface being made of a single element forming discontinuous or non-planar contact surfaces
- B65D19/0016—Rigid pallets without side walls the load supporting surface being made of a single element forming a continuous plane contact surface the base surface being made of a single element forming discontinuous or non-planar contact surfaces and each contact surface having a stringer-like shape
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00014—Materials for the load supporting surface
- B65D2519/00034—Plastic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00049—Materials for the base surface
- B65D2519/00069—Plastic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00084—Materials for the non-integral separating spacer
- B65D2519/00104—Plastic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00119—Materials for the construction of the reinforcements
- B65D2519/00124—Paper
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00119—Materials for the construction of the reinforcements
- B65D2519/00129—Metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00119—Materials for the construction of the reinforcements
- B65D2519/00134—Wood
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00009—Materials
- B65D2519/00119—Materials for the construction of the reinforcements
- B65D2519/00139—Plastic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00263—Overall construction of the pallet
- B65D2519/00273—Overall construction of the pallet made of more than one piece
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00283—Overall construction of the load supporting surface
- B65D2519/00288—Overall construction of the load supporting surface made of one piece
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00313—Overall construction of the base surface
- B65D2519/00318—Overall construction of the base surface made of one piece
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00313—Overall construction of the base surface
- B65D2519/00328—Overall construction of the base surface shape of the contact surface of the base
- B65D2519/00333—Overall construction of the base surface shape of the contact surface of the base contact surface having a stringer-like shape
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00368—Overall construction of the non-integral separating spacer
- B65D2519/00373—Overall construction of the non-integral separating spacer whereby at least one spacer is made of one piece
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00398—Overall construction reinforcements
- B65D2519/00402—Integral, e.g. ribs
- B65D2519/00412—Integral, e.g. ribs on the base surface
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00398—Overall construction reinforcements
- B65D2519/00432—Non-integral, e.g. inserts
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00258—Overall construction
- B65D2519/00398—Overall construction reinforcements
- B65D2519/00432—Non-integral, e.g. inserts
- B65D2519/00447—Non-integral, e.g. inserts on the non-integral separating spacer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00547—Connections
- B65D2519/00552—Structures connecting the constitutive elements of the pallet to each other, i.e. load supporting surface, base surface and/or separate spacer
- B65D2519/00557—Structures connecting the constitutive elements of the pallet to each other, i.e. load supporting surface, base surface and/or separate spacer without separate auxiliary elements
- B65D2519/00562—Structures connecting the constitutive elements of the pallet to each other, i.e. load supporting surface, base surface and/or separate spacer without separate auxiliary elements chemical connection, e.g. glued, welded, sealed
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2519/00—Pallets or like platforms, with or without side walls, for supporting loads to be lifted or lowered
- B65D2519/00004—Details relating to pallets
- B65D2519/00736—Details
- B65D2519/008—Drainage means
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49616—Structural member making
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49616—Structural member making
- Y10T29/49618—Restoring existing member, e.g., reinforcing, repairing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49718—Repairing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
Definitions
- the present invention relates to a method for reinforcing made of a composite material which meets various tow fork impact requirements.
- Pallets are a common device used for stowing and transporting items during shipping. Pallets typically consist of a top deck, a bottom skid, and several supports positioned in between such that there is space between the top deck and bottom skid. The space allows for the tow forks of a fork lift truck to be positioned in between the top deck and bottom skid such that the pallet, and hence anything stowed on the pallet, is able to be lifted and moved from one place to another. This is especially useful when items are being loaded and unloaded during shipping.
- pallets were generally made of wood, but there has been an increasing interest in making pallets out of plastic materials because pallets made of plastic are more durable than pallets made from wood.
- pallets must possess certain strength requirements. More specifically, the supports must be able to withstand the impact from the forks of the fork lift or other vehicle used for moving the pallets, as well as support the load placed on the pallet. Pallets are commonly exposed to impact from the tow forks from a fork lift because they are moved so frequently, and used for transporting various items on essentially a daily basis.
- HDPE high-density polyethylene
- steel roll reinforcement such as steel roll formed sections or pipes to carry loads which are contained within a welded HDPE assembly.
- the present invention relates to a method for reinforcing a post of a pallet used for stowing and transporting items for shipping.
- the pallet design of the present invention uses composite materials such as sheet molding compound (SMC), 40% long glass fiber-filled polypropylene (LGFPP), or 40% long glass fiber-filled high-density polyethylene (LGFHDPE), to eliminate the need for steel reinforcement sections, while still meeting tow fork impact requirements and being economical.
- SMC sheet molding compound
- LGFPP long glass fiber-filled polypropylene
- LGFHDPE long glass fiber-filled high-density polyethylene
- the present invention includes molding the supports, which are typically hollow posts molded using unfilled resins, and then assembling the top deck and bottom skid onto the posts, and applying a weld or adhesive joint to the posts to complete the assembly.
- One object of this invention is to develop an economical approach of reinforcing pallet posts to absorb tow fork impact.
- the present invention is a method with the features of claim 1.
- Figure 1 is an exploded perspective view of a pallet
- Figure 2 is a sectional side view of a support used for the pallet of Figure 1 ;
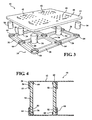
- Figure 3 is an exploded perspective view of the pallet of Figure 1
- Figure 4 is a sectional side view of a support used for a pallet
- Figure 5 is an exploded perspective view of a pallet according to the present invention.
- Figure 6 is a sectional side view of a support used for a pallet, according to the present invention.
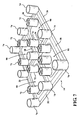
- Figure 7 is a perspective view of a bottom skid and support reinforcements, according to the present invention.
- a first embodiment of a pallet is shown in Figures 1 and 2 generally at 10.
- the pallet 10 includes a top deck 12, a bottom skid 14, and a plurality of supports, or in this embodiment, posts 16.
- Disposed within the posts 16 are reinforcements 18.
- the posts 16 are integrated or molded with the bottom skid 14, but it is within the scope of the invention that the posts 16 may be integrated with the top deck 12 instead of the bottom skid 14.
- the posts have an outer wall 20 and a shorter inner wall 22, and the walls 20,22 form a first circular inner groove 24, which the reinforcement 18 is received into.
- the reinforcements 18 are cylindrical and hollow, allowing each reinforcement 18 to be received into one of the respective grooves 24 of one of the posts 16.
- the bottom skid 14 includes a plurality of cross members, which are substantially perpendicular to one another. More specifically, there is a first cross member 26, a second cross member 28, a third cross member 30, which are perpendicular to a fourth cross member 32, a fifth cross member 34, and a sixth cross member 36. There is a ribbed portion, or raised portion 38 formed as part of each of the cross members 26,28,30,32,34,36 used for providing added strength to the bottom skid 14 as the skid 14 is formed during the injection molding process.
- the inner wall 22 of the post 16 may be of a shorted height compared to the ribbed portion 38, if desired.
- apertures 40 and slots 42 which are used for attaching items to the top deck 12, as well as allowing sprinkler water to drain through a stack of pallets 10 in case of a fire in a warehouse where a group of the pallets 10 are being stored.
- the reinforcements 18 are inserted into the posts 16 as shown in Figure 2 , such that each reinforcement 18 is received into a respective groove 24, as mentioned above.
- the outer wall 20 substantially surrounds the reinforcement 18, best seen in Figure 2 .
- the top deck 12 is then assembled to the posts 16.
- the top deck 12 has a plurality of collars 44 which receive the posts 16 and reinforcements 18.
- the collars 44 include an outer wall 46 and an inner wall 48, with the outer wall 46 extending downwardly further than the inner wall 46.
- the outer wall 46 and inner wall 48 form a second circular inner groove 50, which receives both the post 16 and the reinforcement 18, as shown in Figure 2 .
- connection point 52 is formed between the outer wall 20 of the post 16 and the outer wall 44 to connect the post 16 and the top deck 12.
- the connection point 52 is a thermoplastic weld or adhesive joint, this secures the top deck 12 to the posts 16.
- the connection point 52 of the present invention may be any type of thermoplastic weld for assembly, such as, but not limited to, resistive implant welding, laser welding, vibration welding, and the like.
- the reinforcements 18 are made of extruded or injection molded materials. Different types of materials include reclaimed post consumer or industrial waste, and can be made of wood, steel, or the like. Reclaimed wound paper core of significant thickness is suitable as well.
- the posts 16 provide the proper amount of spacing between the top deck 12 and the bottom skid 14 to allow the tow forks of a fork lift (not shown) to be placed in between the deck 12 and skid 14, allowing the pallet 10 to be moved from one location to another.
- FIG. 3 and 4 A second embodiment of a pallet not forming part of the present invention is shown in Figures 3 and 4 , where like numbers refer to like elements.
- This embodiment has different posts 54 compared to what is shown in the first embodiment.
- the posts 54 are separate components from both the top deck 12 and the bottom skid 14, and both the top deck 12 and bottom skid 14 have collars 56,64 designed to receive the posts 54.
- the collars 56,64 in this embodiment are similar to the collars 44 shown in Figure 2 . More specifically, there is a plurality of upper collars 56 formed as part of the top deck 12, each having an outer wall 58 and an inner wall 60, and the walls 58,60 form a third circular inner groove 62.
- each of the collars 64 having an outer wall 66 and inner wall 68, and the walls 66,68 form a fourth circular inner groove 70.
- the posts 54 are made of an extruded pipe section with a single polymer, and are flame retardant. However, the posts 54 in this embodiment may be co-extruded pipe section with dissimilar materials on different layers of the pipe, such as flame retardant, UV stabilizers, polypropylene, or colorants on the outer layer and raw HDPE on the inner layer. Glass fillers may also be used.
- the posts 54 in this embodiment are thicker such that a reinforcement is not necessary. Additionally, since the posts 54 are not molded using the same injection molding process as the top deck 12 and bottom skid 14, the molding cycle time is not affected.
- a pallet 10 according to the present invention is shown in Figures 5-7 , where like numbers refer to like elements. Reinforcements are included, wherein the reinforcements 72 in this embodiment are made of the same material as the top deck 12 and bottom skid 14.
- the posts 74 are integrally formed with the bottom skid 14, and in a similar manner to the previous embodiments, include an outer wall 76 and an inner wall 78, which form a fifth circular inner groove 80.
- the posts 74 may be integrally formed with the top deck 12, instead of the bottom skid 14.
- the top deck 12 also has a plurality of collars 82 having an outer wall 84 and an inner wall 86, which form a sixth circular inner groove 88.
- the reinforcement 72 is received into the fifth circular inner groove 80, and the ends of both the reinforcement 72 and the posts 74 are received into the sixth circular inner groove 88, best shown in Figure 6 .
- the reinforcements 72 are formed using voids 90 in the area of the mold that is used for creating the bottom skid 14 and posts 74.
- the bottom skid 14 includes the raised portion 38 to provide the proper amount of strength, while reducing material usage, and therefore reducing weight.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Pallets (AREA)
Description
- The present invention relates to a method for reinforcing made of a composite material which meets various tow fork impact requirements.
- Pallets are a common device used for stowing and transporting items during shipping. Pallets typically consist of a top deck, a bottom skid, and several supports positioned in between such that there is space between the top deck and bottom skid. The space allows for the tow forks of a fork lift truck to be positioned in between the top deck and bottom skid such that the pallet, and hence anything stowed on the pallet, is able to be lifted and moved from one place to another. This is especially useful when items are being loaded and unloaded during shipping.
- In the past, pallets were generally made of wood, but there has been an increasing interest in making pallets out of plastic materials because pallets made of plastic are more durable than pallets made from wood. However,
- pallets must possess certain strength requirements. More specifically, the supports must be able to withstand the impact from the forks of the fork lift or other vehicle used for moving the pallets, as well as support the load placed on the pallet. Pallets are commonly exposed to impact from the tow forks from a fork lift because they are moved so frequently, and used for transporting various items on essentially a daily basis.
- Attempts to make pallets out of plastic composite materials have proven to be unsuccessful. One of the reasons for this is that in order for the posts to posses the proper amount of strength to resist impact from tow forks, the posts must have a certain thickness; they must be manufactured with a thickness of nine millimeters to possess the proper strength. However, for typical injection molding cycle times, wall stock thicknesses of the posts should be between three and six millimeters. Posts with the typical wall thickness of three to six millimeters (which are common injection molding wall thicknesses), cannot absorb impact from tow forks; the fork penetrates the post upon impact. Conversely, plastic material having a thickness of nine millimeters (which provides sufficient resistance to tow fork impact) requires longer molding cycle times, which is considered undesirable and uneconomical.
- Another approach to solving this problem is to use high-density polyethylene (HDPE), which has the ability to stretch under load applied from tow forks, with an integrated steel roll reinforcement, such as steel roll formed sections or pipes to carry loads which are contained within a welded HDPE assembly. Using this design is often considered undesirable because it is so costly.
- Known shipping pallets and their manufacturing methods are also disclosed in
EP 1 829 787 A1 ,US 2008/236 454 A1 andCH 542 756 A - Accordingly, there exists a need for an improved manufacturing method for making pallets out of a composite material.
- The present invention relates to a method for reinforcing a post of a pallet used for stowing and transporting items for shipping. The pallet design of the present invention uses composite materials such as sheet molding compound (SMC), 40% long glass fiber-filled polypropylene (LGFPP), or 40% long glass fiber-filled high-density polyethylene (LGFHDPE), to eliminate the need for steel reinforcement sections, while still meeting tow fork impact requirements and being economical.
- The present invention includes molding the supports, which are typically hollow posts molded using unfilled resins, and then assembling the top deck and bottom skid onto the posts, and applying a weld or adhesive joint to the posts to complete the assembly.
- One object of this invention is to develop an economical approach of reinforcing pallet posts to absorb tow fork impact.
- More specifically, the present invention is a method with the features of claim 1.
- Further areas of applicability of the present invention will become apparent from the detailed description provided hereinafter. It should be understood that the detailed description and specific examples, while indicating the preferred embodiment of the invention, are intended for purposes of illustration only and are not intended to limit the scope of the invention.
- The present invention will become more fully understood from the detailed description and the accompanying drawings, wherein:
-
Figure 1 is an exploded perspective view of a pallet, -
Figure 2 is a sectional side view of a support used for the pallet ofFigure 1 ; -
Figure 3 is an exploded perspective view of the pallet ofFigure 1 -
Figure 4 is a sectional side view of a support used for a pallet, -
Figure 5 is an exploded perspective view of a pallet according to the present invention; -
Figure 6 is a sectional side view of a support used for a pallet, according to the present invention; and -
Figure 7 is a perspective view of a bottom skid and support reinforcements, according to the present invention. - The following description is merely exemplary in nature and is in no way intended to limit the invention, its application, or uses.
- A first embodiment of a pallet is shown in
Figures 1 and 2 generally at 10. Thepallet 10 includes atop deck 12, abottom skid 14, and a plurality of supports, or in this embodiment,posts 16. Disposed within theposts 16 arereinforcements 18. In this embodiment, theposts 16 are integrated or molded with thebottom skid 14, but it is within the scope of the invention that theposts 16 may be integrated with thetop deck 12 instead of thebottom skid 14. The posts have anouter wall 20 and a shorterinner wall 22, and thewalls inner groove 24, which thereinforcement 18 is received into. In this embodiment, thereinforcements 18 are cylindrical and hollow, allowing eachreinforcement 18 to be received into one of therespective grooves 24 of one of theposts 16. - During the manufacturing process, the
top deck 12 andbottom skid 14 are formed using an injection molding process. Thebottom skid 14 includes a plurality of cross members, which are substantially perpendicular to one another. More specifically, there is afirst cross member 26, asecond cross member 28, athird cross member 30, which are perpendicular to afourth cross member 32, afifth cross member 34, and asixth cross member 36. There is a ribbed portion, or raisedportion 38 formed as part of each of thecross members bottom skid 14 as theskid 14 is formed during the injection molding process. In one embodiment, theinner wall 22 of thepost 16 may be of a shorted height compared to the ribbedportion 38, if desired. - Additionally, there are
various apertures 40 andslots 42 which are used for attaching items to thetop deck 12, as well as allowing sprinkler water to drain through a stack ofpallets 10 in case of a fire in a warehouse where a group of thepallets 10 are being stored. - Once the
top deck 12, bottom skid 14, andposts 16 are formed, thereinforcements 18 are inserted into theposts 16 as shown inFigure 2 , such that eachreinforcement 18 is received into arespective groove 24, as mentioned above. When assembled, theouter wall 20 substantially surrounds thereinforcement 18, best seen inFigure 2 . Thetop deck 12 is then assembled to theposts 16. In this embodiment, thetop deck 12 has a plurality ofcollars 44 which receive theposts 16 andreinforcements 18. Thecollars 44 include anouter wall 46 and aninner wall 48, with theouter wall 46 extending downwardly further than theinner wall 46. Theouter wall 46 andinner wall 48 form a second circularinner groove 50, which receives both thepost 16 and thereinforcement 18, as shown inFigure 2 . - A
connection point 52 is formed between theouter wall 20 of thepost 16 and theouter wall 44 to connect thepost 16 and thetop deck 12. In this embodiment, theconnection point 52 is a thermoplastic weld or adhesive joint, this secures thetop deck 12 to theposts 16. Theconnection point 52 of the present invention may be any type of thermoplastic weld for assembly, such as, but not limited to, resistive implant welding, laser welding, vibration welding, and the like. Once thetop deck 12 is secured to theposts 16, thepallet 10 is assembled. Because thereinforcements 18 are used, theposts 16 are able to be molded using wall stock thicknesses (which are optimal for providing a thermoplastic weld or adhesive joint) of between three and six millimeters, resulting in no cycle time penalties. - In this embodiment, the
reinforcements 18 are made of extruded or injection molded materials. Different types of materials include reclaimed post consumer or industrial waste, and can be made of wood, steel, or the like. Reclaimed wound paper core of significant thickness is suitable as well. - Once assembled, the
posts 16 provide the proper amount of spacing between thetop deck 12 and thebottom skid 14 to allow the tow forks of a fork lift (not shown) to be placed in between thedeck 12 andskid 14, allowing thepallet 10 to be moved from one location to another. - A second embodiment of a pallet not forming part of the present invention is shown in
Figures 3 and 4 , where like numbers refer to like elements. This embodiment hasdifferent posts 54 compared to what is shown in the first embodiment. Theposts 54 are separate components from both thetop deck 12 and thebottom skid 14, and both thetop deck 12 andbottom skid 14 havecollars posts 54. Thecollars collars 44 shown inFigure 2 . More specifically, there is a plurality ofupper collars 56 formed as part of thetop deck 12, each having anouter wall 58 and aninner wall 60, and thewalls inner groove 62. There is also a plurality oflower collars 64 formed as part of thebottom skid 14, each of thecollars 64 having anouter wall 66 andinner wall 68, and thewalls inner groove 70. Once theposts 54 are disposed in thecollars connection point 52 is used to secure theposts 54 to thetop deck 12 andbottom skid 14. - In this embodiment not forming part of the present invention; there is no reinforcement. The
posts 54 are made of an extruded pipe section with a single polymer, and are flame retardant. However, theposts 54 in this embodiment may be co-extruded pipe section with dissimilar materials on different layers of the pipe, such as flame retardant, UV stabilizers, polypropylene, or colorants on the outer layer and raw HDPE on the inner layer. Glass fillers may also be used. Theposts 54 in this embodiment are thicker such that a reinforcement is not necessary. Additionally, since theposts 54 are not molded using the same injection molding process as thetop deck 12 andbottom skid 14, the molding cycle time is not affected. - A
pallet 10 according to the present invention is shown inFigures 5-7 , where like numbers refer to like elements. Reinforcements are included, wherein thereinforcements 72 in this embodiment are made of the same material as thetop deck 12 andbottom skid 14. Theposts 74 are integrally formed with thebottom skid 14, and in a similar manner to the previous embodiments, include anouter wall 76 and aninner wall 78, which form a fifth circularinner groove 80. However, it is within the scope of the invention that theposts 74 may be integrally formed with thetop deck 12, instead of thebottom skid 14. - The
top deck 12 also has a plurality ofcollars 82 having anouter wall 84 and aninner wall 86, which form a sixth circularinner groove 88. When assembled, thereinforcement 72 is received into the fifth circularinner groove 80, and the ends of both thereinforcement 72 and theposts 74 are received into the sixth circularinner groove 88, best shown inFigure 6 . - According to the present invention the
reinforcements 72 are formed usingvoids 90 in the area of the mold that is used for creating thebottom skid 14 and posts 74. In this and all of the other embodiments, thebottom skid 14 includes the raisedportion 38 to provide the proper amount of strength, while reducing material usage, and therefore reducing weight. Once thereinforcements 72 are formed, they are inserted into theposts 74, and theposts 74 are connected to thetop deck 12 through the use of a thermoplastic weld or adhesive joint 52. Using thereinforcements 72 in this manner does not have an effect on the molding cycle times of thebottom skid 14 and thetop deck 12, while at the same time thereinforcements 72 provide for theposts 74 to have a sufficient amount of strength. - The description of the invention is merely exemplary in nature.
Claims (11)
- A method for reinforcing a post (16) formed as part of a shipping pallet (10), comprising the steps of:providing a top deck (12);providing a bottom skid (14);providing at least one post (16);integrally forming at least one collar (44) with one of said top deck (12) or said bottom skid (14);at least partially inserting said at least one post (16) into said at least one collar (44) such that said at least one post (16) separates said top deck (12) from said bottom skid (14);providing at least one reinforcement (18);inserting said at least one reinforcement (18) into said at least one post (16) to increase the strength of said at least one post (16);providing at least one void as part of said bottom skid (14) ; the method being characterised byforming said at least one reinforcement (18) in said at least one void during the molding of said bottom skid (14).
- The method for reinforcing a post formed as part of a shipping pallet of claim 1, further comprising the steps of:providing at least one collar (44) to be further comprised of a plurality of collars (44) integrally formed as part of said top deck (12);providing said at least one post (16) to be further comprised of a plurality of posts (16) integrally formed as part of said bottom skid (14);positioning at least part of each of said plurality of posts (16) into a respective one of said plurality of collars (44);providing said at least one reinforcement (18) to be further comprised of a plurality of reinforcements (18); anddisposing each of said plurality of reinforcements (18) within a respective one of said plurality of posts (16).
- The method for reinforcing a post formed as part of a shipping pallet of claim 1 or 2, further comprising the steps of:providing at least one collar (44) to be further comprised of a plurality of collars (44) integrally formed as part of said bottom skid (14);providing said at least one post (16) to be further comprised of a plurality of posts (16) integrally formed as part of said top deck (12);positioning at least part of each of said plurality of posts (16) into a respective one of said plurality of collars (44) ;providing said at least one reinforcement (18) to be further comprised of a plurality of reinforcements (18); anddisposing each of said plurality of reinforcements (18) within a respective one of said plurality of posts (16).
- The method for reinforcing a post formed as part of a shipping pallet of any one of claims 1 to 3, further comprising the steps of:providing an outer wall (20) formed as part of said at least one collar (44);providing an inner wall (22) formed as part of said at least one collar (44);forming at least one groove (24) with said outer wall (20) and said inner wall (22);inserting at least a portion of said at least one post (16) and said at least one reinforcement (18) into said at least one groove (24); andproviding a connection point (52) to connect said at least one post (16) to said outer wall (20).
- The method for reinforcing a post formed as part of a shipping pallet of any one of claims 1 to 4, further comprising the steps of:making said at least one reinforcement (18) from one selected from the group consisting of reclaimed post (16) consumer waste, reclaimed post (16) industrial waste, wood, steel, reclaimed wound paper core, and combinations thereof.
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:providing said at least one collar (44) to be further comprised of a plurality of collars (44);forming a portion of said plurality of collars (44) as part of said top deck (12);forming a portion of said plurality of collars (44) as part of said bottom skid (14);providing said at least one post (16) to be further comprised of a plurality of posts (16);extending each of said plurality of posts (16) into one of said plurality of collars (44) formed as part of said top deck (12); andextending each of said plurality of posts (16) into one of said plurality of collars (44) formed as part of said bottom skid (14).
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:providing an outer wall (20) formed as part of said at least one collar (44);providing an inner wall (22) formed as part of said at least one collar (44);forming at least one groove (24) with said outer wall (20) and said inner wall (22);inserting at least a portion of said at least one post (16) into said at least one groove (24); andproviding a connection point (52) to connect said at least one post (16) to said outer wall (20).
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:providing at least one cross member (26) formed part of said bottom skid (14);integrally forming said at least one post (16) as part of said at least one cross member (26).
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:forming a ribbed portion as part of said at least one cross member (26).
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:forming at least one cross member (26) as part of said bottom skid (14); andintegrally forming said at least one collar (44) as part of said at least one cross member (26).
- The method for reinforcing a post (16) formed as part of a shipping pallet (10) of claim 1, further comprising the steps of:providing at least one aperture (40) formed as part of said top deck (12); andproviding at least one slot (42) formed as part of said top deck (12), both of said at least one aperture (40) and said at least one slot (42) operable for allowing liquid to drain from said top deck (12).
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US27978509P | 2009-10-26 | 2009-10-26 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2314517A1 EP2314517A1 (en) | 2011-04-27 |
| EP2314517B1 true EP2314517B1 (en) | 2013-03-06 |
Family
ID=43416291
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP10013968A Not-in-force EP2314517B1 (en) | 2009-10-26 | 2010-10-26 | Method for reinforcing a post of a shipping pallet |
Country Status (3)
| Country | Link |
|---|---|
| US (2) | US20110259248A1 (en) |
| EP (1) | EP2314517B1 (en) |
| CA (1) | CA2717517C (en) |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA2717517C (en) | 2009-10-26 | 2017-11-28 | Magna International Inc. | Shipping pallet post reinforcement |
| AU2011246970A1 (en) * | 2010-04-08 | 2012-11-01 | Magna International Inc. | Shipping pallet post reinforcement |
| JP5627532B2 (en) * | 2011-04-15 | 2014-11-19 | 三甲株式会社 | Box pallet and side wall of box pallet |
| AR104936A1 (en) | 2015-06-08 | 2017-08-23 | Rehrig Pacific Co | PALLET ASSEMBLY |
| US9745097B2 (en) | 2015-10-02 | 2017-08-29 | Pallets.Com Llc | Pallet support block and a pallet constructed with pallet support blocks |
| US9359109B1 (en) * | 2015-10-02 | 2016-06-07 | Palets.com LLC | Pallet support block and a pallet constructed with pallet support blocks |
| US9776762B2 (en) | 2016-01-06 | 2017-10-03 | Chep Technology Pty Limited | Pallet with extruded composite support blocks and associated methods of making the same |
| US10081453B2 (en) * | 2016-11-21 | 2018-09-25 | Chep Technology Pty Limited | Plastic pallet with support blocks having upper towers and associated methods |
| DE102017107237A1 (en) * | 2017-04-04 | 2018-10-04 | Schoeller Allibert Gmbh | Plastic pallet with stiffening elements |
| US10562666B2 (en) | 2018-05-31 | 2020-02-18 | Chep Technology Pty Limited | Repairable plastic pallet with grommets in the top deck and associated methods |
| WO2020028539A1 (en) * | 2018-07-31 | 2020-02-06 | Igps Logistics, Llc | Plastic pallet having an integrally formed deck and method of manufacturing the same |
Family Cites Families (24)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH542756A (en) * | 1972-02-23 | 1973-10-15 | Bolliger Werner | palette |
| FR2590870B1 (en) * | 1985-12-04 | 1988-06-24 | Allibert Sa | REINFORCED LOADING PALLET AND METHOD FOR REINFORCING SUCH A PALLET |
| US5413052A (en) * | 1991-08-05 | 1995-05-09 | Trienda Corporation | Plastic pallet with two decks |
| US5197396A (en) * | 1991-08-05 | 1993-03-30 | Penda Corporation | Double deck plastic pallet |
| US5367961A (en) * | 1992-10-28 | 1994-11-29 | Arai; Hiroshi | Pallet support leg including semi-circular flange blades |
| US5483899A (en) * | 1994-07-05 | 1996-01-16 | Christie; Eugene P. | Modular pallet arrangement |
| US5492069A (en) * | 1994-07-18 | 1996-02-20 | E. I. Du Pont De Nemours And Company | Pallet assembly |
| US6199488B1 (en) * | 1997-10-07 | 2001-03-13 | James Favaron | Reinforced plastic pallets |
| US6283044B1 (en) * | 1998-07-01 | 2001-09-04 | Rehrig Pacific Company | Pallet assembly |
| US6446563B1 (en) * | 1998-10-07 | 2002-09-10 | Harout Ohanesian | Thermoplastic pallet |
| US6564725B2 (en) * | 2001-01-05 | 2003-05-20 | Ronald G. Hale | Load supporting platform |
| US6807910B2 (en) * | 2001-10-19 | 2004-10-26 | Rehrig Pacific Company | Pallet assembly |
| US6998433B2 (en) * | 2003-02-27 | 2006-02-14 | Rehig Pacific Company | Flame retardant polyolefin pallets and flame retardant master batch for their production |
| US7086339B2 (en) * | 2003-04-29 | 2006-08-08 | Rehrig Pacific Company | Pallet assembly |
| US7921784B2 (en) * | 2004-07-29 | 2011-04-12 | Rehrig Pacific Company | Snap-together pallet |
| US7779765B2 (en) * | 2006-03-03 | 2010-08-24 | Daniel Kelly | Pallet with telescoped leg assemblies |
| US7779764B2 (en) * | 2006-05-08 | 2010-08-24 | Chep Technology Pty Limited | Durable pallet and pallet block |
| US7748329B2 (en) * | 2006-07-24 | 2010-07-06 | Rehrig Pacific Company | Pallet assembly |
| US8141500B2 (en) * | 2007-03-30 | 2012-03-27 | Chep Technology Pty Limited | Plastic pallet with sleeved reinforcing rods and associated method for making the same |
| USD584874S1 (en) | 2008-02-14 | 2009-01-13 | Magna Marque International Inc. | Load bearing pallet |
| US20100229765A1 (en) * | 2009-03-10 | 2010-09-16 | Bryan Shafer | Industrial pallets formed of recycled and/or scrap lumber and method of manufacturing |
| US20110120353A1 (en) * | 2009-09-22 | 2011-05-26 | Guy Jensen | Plastic rackable pallet |
| CA2717517C (en) | 2009-10-26 | 2017-11-28 | Magna International Inc. | Shipping pallet post reinforcement |
| US20110259249A1 (en) * | 2010-04-22 | 2011-10-27 | Ogburn Sean T | Pallet |
-
2010
- 2010-10-13 CA CA2717517A patent/CA2717517C/en not_active Expired - Fee Related
- 2010-10-22 US US12/910,403 patent/US20110259248A1/en not_active Abandoned
- 2010-10-26 EP EP10013968A patent/EP2314517B1/en not_active Not-in-force
-
2012
- 2012-12-27 US US13/727,853 patent/US9038273B2/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| CA2717517A1 (en) | 2011-04-26 |
| EP2314517A1 (en) | 2011-04-27 |
| US20110259248A1 (en) | 2011-10-27 |
| US20130111724A1 (en) | 2013-05-09 |
| CA2717517C (en) | 2017-11-28 |
| US9038273B2 (en) | 2015-05-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2717517C (en) | Shipping pallet post reinforcement | |
| EP2555989B1 (en) | Shipping pallet comprising reinforced posts | |
| EP2015651B1 (en) | Pallet | |
| US8127691B2 (en) | SMC pallet | |
| RU2152894C2 (en) | Thermoplastic pallet | |
| US20110120353A1 (en) | Plastic rackable pallet | |
| US20100043676A1 (en) | Pallet with alignment features | |
| US20020043184A1 (en) | Method of reinforcing a plastic pallet | |
| US20090095205A1 (en) | Plastic pallet system | |
| JP2000203578A (en) | Synthetic resin pallets | |
| AU2008237596A1 (en) | Improved Pallet | |
| HUP0102819A2 (en) | Pallet assembly | |
| EP1973788A2 (en) | Rackable twin sheet pallet | |
| US10118731B2 (en) | Pallet assembly | |
| US20060081158A1 (en) | Pultrusion pallet | |
| WO2016154260A1 (en) | Apparatus and methods directed towards a plastic pallet | |
| KR20160149443A (en) | Paper pallet | |
| US20240367852A1 (en) | Structurally hardened pallet assembly and components | |
| KR101769697B1 (en) | Palet | |
| CZ37704U1 (en) | Composite pallet | |
| AU776023B2 (en) | A pallet | |
| US20230211920A1 (en) | Pallet with internal frame | |
| KR200270474Y1 (en) | Leg-mounted integrated steel pallet | |
| KR20140010220A (en) | Palette process of manufacture and palette | |
| AU2016204316A1 (en) | Pallet assembly |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17P | Request for examination filed |
Effective date: 20111019 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 599462 Country of ref document: AT Kind code of ref document: T Effective date: 20130315 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602010005160 Country of ref document: DE Effective date: 20130502 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 599462 Country of ref document: AT Kind code of ref document: T Effective date: 20130306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130606 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130617 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130606 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20130306 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130607 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130706 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130708 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| 26N | No opposition filed |
Effective date: 20131209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602010005160 Country of ref document: DE Effective date: 20131209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131026 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20101026 Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602010005160 Country of ref document: DE Representative=s name: GLAWE DELFS MOLL PARTNERSCHAFT MBB VON PATENT-, DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130306 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20181016 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20181024 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20190913 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602010005160 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200501 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20191026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 |