EP1985820B1 - Heat-resistant cast steel exhaust manifold - Google Patents
Heat-resistant cast steel exhaust manifold Download PDFInfo
- Publication number
- EP1985820B1 EP1985820B1 EP07714523A EP07714523A EP1985820B1 EP 1985820 B1 EP1985820 B1 EP 1985820B1 EP 07714523 A EP07714523 A EP 07714523A EP 07714523 A EP07714523 A EP 07714523A EP 1985820 B1 EP1985820 B1 EP 1985820B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- thickness
- flanges
- exhaust manifold
- ports
- heat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/18—Construction facilitating manufacture, assembly, or disassembly
- F01N13/1805—Fixing exhaust manifolds, exhaust pipes or pipe sections to each other, to engine or to vehicle body
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/08—Other arrangements or adaptations of exhaust conduits
- F01N13/10—Other arrangements or adaptations of exhaust conduits of exhaust manifolds
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/22—Moulds for peculiarly-shaped castings
- B22C9/24—Moulds for peculiarly-shaped castings for hollow articles
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/08—Other arrangements or adaptations of exhaust conduits
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/18—Construction facilitating manufacture, assembly, or disassembly
- F01N13/1861—Construction facilitating manufacture, assembly, or disassembly the assembly using parts formed by casting or moulding
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N2450/00—Methods or apparatus for fitting, inserting or repairing different elements
- F01N2450/22—Methods or apparatus for fitting, inserting or repairing different elements by welding or brazing
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N2530/00—Selection of materials for tubes, chambers or housings
Definitions
- the present invention relates to an exhaust manifold made of heat-resistant cast steel, which can be produced with a small number of steps at a high yield, and has small weight and excellent thermal deformation resistance.
- the exhaust manifold for gathering an exhaust gas from an engine and sending it to an exhaust pipe comprises pluralities of flanges each having a hole connected to each exhaust port of a cylinder head of an engine with bolts, a port connected to each flange, and a convergence portion in which pluralities of ports are converging.
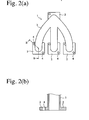
- the flanges are generally thicker than the ports in the exhaust manifold ( Fig. 2 ) as described in JP 10-26018 A .
- the flanges have an average thickness of about 12 mm, and the ports have an average thickness of about 5 mm.
- voids are likely generated in the finally solidified flanges.
- US 6,256, 950B1 discloses another exhaust manifold which is integrally cast with a turbine housing for a turbocharger.
- each flange is provided with a riser 6 as shown in Fig. 3 , so that a melt is supplied to the flange during solidification.
- risers are not used as part of the products, resulting in a lower yield per the melt used. Further, risers should be removed after casting, a larger number of steps is needed.
- an object of the present invention is to provide an exhaust manifold made of heat-resistant cast steel, which can be produced with a small number of steps at a high yield, and has small weight and excellent thermal deformation resistance.
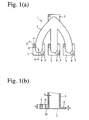
- Fig. 1(a) is a schematic plan view showing an exhaust manifold made of heat-resistant cast steel.
- Fig. 1 (b) is a cross-sectional view taken along the line A-A in Fig. 1(a) .
- Fig. 2(a) is a schematic plan view showing a conventional exhaust manifold.
- Fig. 2(b) is a cross-sectional view taken along the line B-B in Fig. 2(a) .
- Fig. 3 is a schematic view showing a riser provided for casting a conventional exhaust manifold.
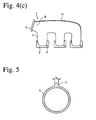
- Fig. 4(a) is a schematic plan view showing an example of the exhaust manifolds of the present invention made of heat-resistant cast steel.
- Fig. 4(b) is a schematic front view showing another example of the exhaust manifolds of the present invention made of heat-resistant cast steel.
- Fig. 4(c) is a schematic side view showing a further example of the exhaust manifolds of the present invention made of heat-resistant cast steel.
- Fig. 5 is a cross-sectional view showing a ridge.
- the thickness of flanges, ports and bolthole-surrounding portions is expressed by an average value.
- the bolthole-surrounding portion in the flange has a thickness t 3 as shown in Fig. 1(b) .
- the ridge has a thickness t 4 in a cross section perpendicular to a longitudinal direction as shown in Fig. 5 .
- each flange 2 need not be provided with a riser, making it possible to produce the exhaust manifold with a smaller number of steps at a higher yield.
- the thickness of the flanges 2 is less than 80% of that of the ports 3, the flanges 2 are not easily filled with a melt, resulting in insufficient melt flow.
- the flanges 2 are more than 150% as thick as the ports 3, the flanges 2 are likely to have voids.
- the flanges 2 are preferably 85-130% as thick as the ports 3.
- each flange 2 and the surrounding portion 5 of each bolthole 4 after casting and before machining are thicker by a predetermined machining margin 7
- the thickness t 1 of the flange 2 and the thickness t 3 of the surrounding portion 5 of the bolthole 4 are expressed as thickness from the surface 21 of the flange 2 after machining in the present invention, as shown in Fig. 1(b) .
- the thickness of the surrounding portions 5 of the boltholes 4 is 110-300% of that of the flanges 2, the flanges 2 are not easily thermally deformed even if the exhaust manifold is exposed to a high-temperature exhaust gas. Thus, an exhaust gas is prevented from flowing out through gaps between the exhaust ports of a cylinder head and the flanges 2 of the exhaust manifold.
- the surrounding portions 5 of the boltholes 4 are less than 110% as thick as the flanges 2, the flanges 2 are easily thermally deformed by a high-temperature exhaust gas. When it exceeds 300%, voids are likely generated in the flanges 2 during casting.
- the ports 3 are not thermally deformed even if exposed to a high-temperature exhaust gas, thereby preventing an exhaust gas from leaking.
- the thickness t 4 of the ridge 11 is preferably 70-140% as thick as the port 3. When t 4 is less than 70% of the thickness of the ports 3, the thermal deformation of the ports 3 cannot be sufficiently prevented. When t 4 exceeds 140%, the exhaust manifold cannot be made light in weight.
- the thickness t 4 of the ridges 11 is preferably 80-120% as thick as the ports 3.
- the ridges 11 may extend from the convergence portion 8 to the branching portions of the ports 3 as shown in Figs. 4(b) and 4(c) .
- the heat-resistant-cast-steel-made exhaust manifold of the present invention is preferably made of, for instance, heat-resistant, austenitic cast steel comprising by mass 0.2-1.0% of C, 0.05-0.6% of (C-Nb/8), 2% or less of Si, 2% or less of Mn, 8-20% of Ni, 15-30% of Cr, 0.5-6.0% of Nb, 1-6% of W, 0.01-0.3% of N, and 0.01-0.5% of S, the balance being Fe and inevitable impurities.
- Exhaust manifolds shown in Fig. 1 were formed by heat-resistant, austenitic cast steel having a composition comprising by mass 0.45% of C, 1.2% of Si, 1.0% of Mn, 0.015% of P, 0.015% of S, 10% of Ni, 20% of Cr, 1.5% of Nb, and 3.0% of W (Examples 1-8 and Comparative Examples 1-3).
- the thickness t 1 of a flange 2, the thickness t 2 of a port 3, and the thickness t 3 of an surrounding portion 5 of a bolthole 4 are shown in Table 1.
- Exhaust manifolds shown in Fig. 4(a) were also formed by the same heat-resistant, austenitic cast steel as above (Examples 9-14).
- the thickness t 4 of ridges 11 is shown in Table 1 together with t 1 to t 3 .
- Each exhaust manifold was connected to exhaust ports of a cylinder head of a usual engine, to evaluate the thermal deformation of flanges when the engine was operated.
- the exhaust manifolds of the present invention having flanges 80-150% as thick as ports were produced free from voids without providing risers, and suffered only small thermal deformation during use.
- Examples 1, 2 and 4-8 in which the bolthole-surrounding portions were 110-300% as thick as the flanges, suffered small thermal deformation.
- the exhaust manifolds of Examples 9-14 each having ridges extending along the ports from the convergence portion suffered smaller thermal deformation.
- the exhaust manifold of the present invention made of heat-resistant cast steel and having the above structure, which has small weight and excellent thermal deformation resistance, can be efficiently produced with a small number of steps.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Combustion & Propulsion (AREA)
- General Engineering & Computer Science (AREA)
- Exhaust Silencers (AREA)
Description
- The present invention relates to an exhaust manifold made of heat-resistant cast steel, which can be produced with a small number of steps at a high yield, and has small weight and excellent thermal deformation resistance.
- The exhaust manifold for gathering an exhaust gas from an engine and sending it to an exhaust pipe comprises pluralities of flanges each having a hole connected to each exhaust port of a cylinder head of an engine with bolts, a port connected to each flange, and a convergence portion in which pluralities of ports are converging. To prevent the thermal deformation of flanges by a high-temperature exhaust gas, the flanges are generally thicker than the ports in the exhaust manifold (
Fig. 2 ) as described inJP 10-26018 A US 6,256, 950B1 discloses another exhaust manifold which is integrally cast with a turbine housing for a turbocharger. - As automobile engines are recently required to have increasingly higher performance and fuel efficiency, an exhaust gas temperature has been elevating. To secure high-temperature strength and oxidation resistance at 900°C or higher, the exhaust manifold is made of heat-resistant cast steel. However, voids are likely to generate because the cast steel suffers large solidification shrinkage during casting. To cope with this problem, each flange is provided with a
riser 6 as shown inFig. 3 , so that a melt is supplied to the flange during solidification. However, risers are not used as part of the products, resulting in a lower yield per the melt used. Further, risers should be removed after casting, a larger number of steps is needed. - Accordingly, an object of the present invention is to provide an exhaust manifold made of heat-resistant cast steel, which can be produced with a small number of steps at a high yield, and has small weight and excellent thermal deformation resistance.
- The exhaust manifold according to
claim 1 of the present invention solves the above-mentioned problems -
Fig. 1(a) is a schematic plan view showing an exhaust manifold made of heat-resistant cast steel. -
Fig. 1 (b) is a cross-sectional view taken along the line A-A inFig. 1(a) . -
Fig. 2(a) is a schematic plan view showing a conventional exhaust manifold. -
Fig. 2(b) is a cross-sectional view taken along the line B-B inFig. 2(a) . -
Fig. 3 is a schematic view showing a riser provided for casting a conventional exhaust manifold. -
Fig. 4(a) is a schematic plan view showing an example of the exhaust manifolds of the present invention made of heat-resistant cast steel. -
Fig. 4(b) is a schematic front view showing another example of the exhaust manifolds of the present invention made of heat-resistant cast steel. -
Fig. 4(c) is a schematic side view showing a further example of the exhaust manifolds of the present invention made of heat-resistant cast steel. -
Fig. 5 is a cross-sectional view showing a ridge. - In the present invention, the thickness of flanges, ports and bolthole-surrounding portions is expressed by an average value. The bolthole-surrounding portion in the flange has a thickness t3 as shown in
Fig. 1(b) . The ridge has a thickness t4 in a cross section perpendicular to a longitudinal direction as shown inFig. 5 . - As shown in
Fig. 1 , because theflanges 2 are 80-150% as thick as theports 3, theflanges 2, finally solidified portions, are less likely to have voids. Accordingly, eachflange 2 need not be provided with a riser, making it possible to produce the exhaust manifold with a smaller number of steps at a higher yield. When the thickness of theflanges 2 is less than 80% of that of theports 3, theflanges 2 are not easily filled with a melt, resulting in insufficient melt flow. When theflanges 2 are more than 150% as thick as theports 3, theflanges 2 are likely to have voids. Theflanges 2 are preferably 85-130% as thick as theports 3. Although eachflange 2 and the surroundingportion 5 of eachbolthole 4 after casting and before machining are thicker by apredetermined machining margin 7, the thickness t1 of theflange 2 and the thickness t3 of the surroundingportion 5 of thebolthole 4 are expressed as thickness from thesurface 21 of theflange 2 after machining in the present invention, as shown inFig. 1(b) . - Because the thickness of the surrounding
portions 5 of theboltholes 4 is 110-300% of that of theflanges 2, theflanges 2 are not easily thermally deformed even if the exhaust manifold is exposed to a high-temperature exhaust gas. Thus, an exhaust gas is prevented from flowing out through gaps between the exhaust ports of a cylinder head and theflanges 2 of the exhaust manifold. When the surroundingportions 5 of theboltholes 4 are less than 110% as thick as theflanges 2, theflanges 2 are easily thermally deformed by a high-temperature exhaust gas. When it exceeds 300%, voids are likely generated in theflanges 2 during casting. - According to the present invention, when a
ridge 11 extends along eachport 3 from theconvergence portion 8 to eachflange 2 as shown inFig. 4(a) , theports 3 are not thermally deformed even if exposed to a high-temperature exhaust gas, thereby preventing an exhaust gas from leaking. The thickness t4 of theridge 11 is preferably 70-140% as thick as theport 3. When t4 is less than 70% of the thickness of theports 3, the thermal deformation of theports 3 cannot be sufficiently prevented. When t4 exceeds 140%, the exhaust manifold cannot be made light in weight. The thickness t4 of theridges 11 is preferably 80-120% as thick as theports 3. Instead of extending along eachport 3 from theconvergence portion 8 to eachflange 2 as shown inFig. 4(a) , theridges 11 may extend from theconvergence portion 8 to the branching portions of theports 3 as shown inFigs. 4(b) and4(c) . - To have small weight and excellent thermal deformation resistance, the heat-resistant-cast-steel-made exhaust manifold of the present invention is preferably made of, for instance, heat-resistant, austenitic cast steel comprising by mass 0.2-1.0% of C, 0.05-0.6% of (C-Nb/8), 2% or less of Si, 2% or less of Mn, 8-20% of Ni, 15-30% of Cr, 0.5-6.0% of Nb, 1-6% of W, 0.01-0.3% of N, and 0.01-0.5% of S, the balance being Fe and inevitable impurities.
- The present invention will be explained in more detail referring to Examples 9-14 below without intention of restricting the scope of the present invention.
- Examples 1-14 and Comparative Examples 1-3
- Exhaust manifolds shown in
Fig. 1 were formed by heat-resistant, austenitic cast steel having a composition comprising by mass 0.45% of C, 1.2% of Si, 1.0% of Mn, 0.015% of P, 0.015% of S, 10% of Ni, 20% of Cr, 1.5% of Nb, and 3.0% of W (Examples 1-8 and Comparative Examples 1-3). The thickness t1 of aflange 2, the thickness t2 of aport 3, and the thickness t3 of an surroundingportion 5 of abolthole 4 are shown in Table 1. Exhaust manifolds shown inFig. 4(a) were also formed by the same heat-resistant, austenitic cast steel as above (Examples 9-14). The thickness t4 ofridges 11 is shown in Table 1 together with t1 to t3. - With respect to each exhaust manifold, a yield (number of steps), and the thermal deformation of the flanges during use were evaluated as follows: The results are shown in Table 1.
- (1) Evaluation of yield (number of steps)
- Good: Good casting free from voids was conducted without providing a riser to each
flange 2. - Poor: Good casting could not be conducted without providing a riser to each
flange 2. Because the risers were used, they had to be cut after casting. - (2) Each exhaust manifold was connected to exhaust ports of a cylinder head of a usual engine, to evaluate the thermal deformation of flanges when the engine was operated.
- Excellent: Thermal deformation did not occur in both of the
ports 3 and theflanges 2. - Good: Thermal deformation did not occur in the
flanges 2, causing no leak of an exhaust gas. - Fair: Thermal deformation occurred slightly in the
flanges 2, but there was no leak of an exhaust gas. - Poor: Thermal deformation occurred in the
flanges 2, causing the leak of an exhaust gas. -

-

- As is clear from Table 1, the exhaust manifolds of the present invention having flanges 80-150% as thick as ports were produced free from voids without providing risers, and suffered only small thermal deformation during use. Examples 1, 2 and 4-8, in which the bolthole-surrounding portions were 110-300% as thick as the flanges, suffered small thermal deformation. The exhaust manifolds of Examples 9-14 each having ridges extending along the ports from the convergence portion suffered smaller thermal deformation.
- The exhaust manifold of the present invention made of heat-resistant cast steel and having the above structure, which has small weight and excellent thermal deformation resistance, can be efficiently produced with a small number of steps.
Claims (2)
- An exhaust manifold made of heat-resistant cast steel comprising:pluralities of flanges (2) each having a hole (4) connectable to an exhaust port of a cylinder head of an engine with bolts;pluralities of ports (3) connected to said flanges (2);a convergence portion (8) in which said ports (3) are converging; anda ridge (11) extending along each port (3) from said convergence portion (8),characterised in thatthe thickness t1 of each flange (2) except its portion surrounding said hole (4) is 80-150% of the wall-thickness t2 of said ports (3);the thickness t3 of the hole-surrounding portion of the flange (2) is 110-300% of said thickness t1; andthe thickness t4 of said ridges (11) is 70-140% of said wall thickness t2 of said ports (3).
- The exhaust manifold according to claim 1, wherein said thickness t1 is 80-100% of said wall-thickness t2.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2006040499 | 2006-02-17 | ||
| PCT/JP2007/052997 WO2007094500A1 (en) | 2006-02-17 | 2007-02-19 | Heat-resistant cast steel exhaust manifold |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1985820A1 EP1985820A1 (en) | 2008-10-29 |
| EP1985820A4 EP1985820A4 (en) | 2010-01-06 |
| EP1985820B1 true EP1985820B1 (en) | 2012-09-05 |
Family
ID=38371671
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP07714523A Ceased EP1985820B1 (en) | 2006-02-17 | 2007-02-19 | Heat-resistant cast steel exhaust manifold |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20090064670A1 (en) |
| EP (1) | EP1985820B1 (en) |
| JP (1) | JPWO2007094500A1 (en) |
| KR (1) | KR20080096666A (en) |
| CN (1) | CN101384803A (en) |
| WO (1) | WO2007094500A1 (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102009011748B4 (en) * | 2009-03-09 | 2013-05-23 | Tenneco Gmbh | Exhaust system for an internal combustion engine with juxtaposed flange plates |
| DE102014103820A1 (en) * | 2014-03-20 | 2015-09-24 | Benteler Automobiltechnik Gmbh | Exhaust manifold for an exhaust system of an internal combustion engine |
| US9488081B2 (en) | 2014-12-17 | 2016-11-08 | Caterpillar Inc. | Exhaust manifold assembly and system |
| EP3730756B1 (en) * | 2019-04-26 | 2021-09-22 | Kubota Corporation | Exhaust system for engine |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4182122A (en) * | 1978-02-15 | 1980-01-08 | Caterpillar Tractor Co. | Insulated exhaust manifold |
| JPS60137112U (en) * | 1984-02-22 | 1985-09-11 | トヨタ自動車株式会社 | exhaust manifold |
| JPS63132825U (en) * | 1987-02-23 | 1988-08-30 | ||
| JP2605242B2 (en) * | 1991-04-17 | 1997-04-30 | 豊田合成株式会社 | Manufacturing method of steering wheel core metal |
| JPH0658120U (en) * | 1991-07-16 | 1994-08-12 | 本田技研工業株式会社 | Exhaust manifold of multi-cylinder engine |
| US5566548A (en) * | 1994-11-09 | 1996-10-22 | Caterpillar Inc. | Exhaust manifold joint |
| JPH1026018A (en) | 1996-07-10 | 1998-01-27 | Nissan Motor Co Ltd | Exhaust manifold of internal combustion engine |
| JPH1162741A (en) * | 1997-08-08 | 1999-03-05 | Suzuki Motor Corp | Engine intake manifold |
| DE19819946A1 (en) * | 1998-05-05 | 1999-11-11 | Boysen Friedrich Gmbh Co Kg | Exhaust manifold |
| JP2000199427A (en) * | 1998-12-28 | 2000-07-18 | Hitachi Metals Ltd | Exhaust manifold with integrated turbine housing casting for turbocharger |
| JP4269244B2 (en) * | 1999-04-14 | 2009-05-27 | 日立金属株式会社 | Casting for exhaust manifold |
| JP2001207841A (en) * | 2000-01-24 | 2001-08-03 | Mitsubishi Motors Corp | Exhaust manifold for multi-cylinder engine |
| JP2002309935A (en) * | 2001-02-08 | 2002-10-23 | Hitachi Metals Ltd | Exhaust system parts of heat-resisting steel |
| JP2003063224A (en) * | 2001-08-29 | 2003-03-05 | Hitachi Metals Ltd | Suspension arm for automobile |
| JP4087320B2 (en) * | 2003-09-12 | 2008-05-21 | 本田技研工業株式会社 | Cylinder block for internal combustion engine |
-
2007
- 2007-02-19 KR KR1020087019988A patent/KR20080096666A/en not_active Ceased
- 2007-02-19 CN CNA2007800056541A patent/CN101384803A/en active Pending
- 2007-02-19 WO PCT/JP2007/052997 patent/WO2007094500A1/en not_active Ceased
- 2007-02-19 JP JP2008500590A patent/JPWO2007094500A1/en active Pending
- 2007-02-19 EP EP07714523A patent/EP1985820B1/en not_active Ceased
- 2007-02-19 US US12/279,482 patent/US20090064670A1/en not_active Abandoned
Also Published As
| Publication number | Publication date |
|---|---|
| CN101384803A (en) | 2009-03-11 |
| WO2007094500A1 (en) | 2007-08-23 |
| US20090064670A1 (en) | 2009-03-12 |
| EP1985820A4 (en) | 2010-01-06 |
| JPWO2007094500A1 (en) | 2009-07-09 |
| KR20080096666A (en) | 2008-10-31 |
| EP1985820A1 (en) | 2008-10-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7959407B2 (en) | Blade outer air seals, cores, and manufacture methods | |
| US7900458B2 (en) | Turbine airfoils with near surface cooling passages and method of making same | |
| US7874792B2 (en) | Blade outer air seals, cores, and manufacture methods | |
| US8528513B2 (en) | Cast steel piston for internal combustion engines | |
| JP4379753B2 (en) | Exhaust system component, internal combustion engine using the same, and method of manufacturing exhaust system component | |
| JP5781520B2 (en) | Fluid-cooled exhaust manifold | |
| JP5062071B2 (en) | Internal combustion engine cylinder block | |
| JPH07286503A (en) | High efficiency gas turbine | |
| US7565800B2 (en) | Exhaust components including high temperature divider plate assemblies | |
| US20020189229A1 (en) | Gas turbine for power generation and combined power generation system | |
| EP1493909B1 (en) | Cylinder head | |
| JPWO2005007914A1 (en) | Austenitic heat-resistant spheroidal graphite cast iron | |
| EP1985820A1 (en) | Heat-resistant cast steel exhaust manifold | |
| WO2016017675A1 (en) | Cylinder head for internal combustion engine | |
| JP2012012959A (en) | Structure for cooling engine | |
| CN112696258B (en) | Control method for thermal deformation design of exhaust manifold | |
| US10781769B2 (en) | Method of manufacturing an engine block | |
| US20080267808A1 (en) | High Alloy Iron, Use of the Material for Structural Components that are Subject to High Thermal Stress and Corresponding Structural Component | |
| KR20150004385A (en) | Metal cast component and method for producing a metal cast component | |
| JP4670610B2 (en) | Intercooler | |
| JP2007285169A (en) | Cylinder head structure of an internal combustion engine with a supercharger | |
| JP6187229B2 (en) | Engine cylinder head structure | |
| CN217518744U (en) | Compound exhaust pipe diesel engine cylinder cover structure | |
| JP2010216461A (en) | Exhaust manifold | |
| JP2005002861A (en) | Piston structure |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20080909 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR IT |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RBV | Designated contracting states (corrected) |
Designated state(s): DE FR IT |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20091203 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B22C 9/24 20060101ALI20091127BHEP Ipc: F01N 7/10 00000000AFI20070921BHEP |
|
| 17Q | First examination report despatched |
Effective date: 20100512 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Ref document number: 602007025269 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: F01N0007100000 Ipc: F01N0013180000 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: F01N 13/18 20100101AFI20120120BHEP Ipc: B22C 9/24 20060101ALI20120120BHEP Ipc: F01N 13/10 20100101ALI20120120BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR IT |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602007025269 Country of ref document: DE Effective date: 20121025 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20130606 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602007025269 Country of ref document: DE Effective date: 20130606 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20211230 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20220111 Year of fee payment: 16 Ref country code: FR Payment date: 20220118 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602007025269 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230219 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230228 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230901 |