EP1853760B1 - Dewatering apparatus - Google Patents
Dewatering apparatus Download PDFInfo
- Publication number
- EP1853760B1 EP1853760B1 EP06716944A EP06716944A EP1853760B1 EP 1853760 B1 EP1853760 B1 EP 1853760B1 EP 06716944 A EP06716944 A EP 06716944A EP 06716944 A EP06716944 A EP 06716944A EP 1853760 B1 EP1853760 B1 EP 1853760B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- wire
- blade
- forming roll
- dewatering
- roll
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images

Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F1/00—Wet end of machines for making continuous webs of paper
- D21F1/48—Suction apparatus
- D21F1/483—Drainage foils and bars
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F9/00—Complete machines for making continuous webs of paper
- D21F9/003—Complete machines for making continuous webs of paper of the twin-wire type
Definitions
- the present invention relates to a dewatering apparatus adapted for use in a twin-wire dewatering section of a paper machine. More specifically it relates to an apparatus comprising a rotating forming roll, a head box for supplying stock, arranged before the forming roll, a closed loop first wire, also called inner wire, adapted to be partly wrapped around the forming roll up to a separation line where its contact with the forming roll ceases, and to receive the stock from the head box on its surface not facing the forming roll, a closed loop second wire, also called outer wire, adapted to be partly wrapped around the forming roll on top of the first wire thereby pressing the stock between itself and the first wire, and a first blade substantially parallel to the forming roll, said blade being arranged to support the roll facing side of the first wire after the separation line from the forming roll and being arranged such that the tip of the blade is directed against the wire transporting direction.
- a closed loop first wire also called inner wire
- outer wire also called outer wire
- One conventional fourdrinier dewatering system for a paper machine comprises table rolls as dewatering elements.
- the limitations of using table rolls as dewatering elements in fourdrinier wire parts appear at high wire speeds.
- the local under pressure generated in the outgoing nip between wire bottom and roll surface then becomes too high. This under pressure will generate a local downward movement of the wire, which thereafter has to move back upwards to the top level of the following table roll.
- the vertical upward movement of the free fibre suspension on top of the wire (and the already dewatered part of the web) will then become so intense that drops form and escape from the suspension surface, which may generate formation disturbances.
- the amplitude of the under pressure pulses generated by the table rolls increases with the square of the wire speed. At wire speeds in excess of approx. 500m/min. the suction pulses will become so intense that the formation deteriorates.
- a further principle of twin-wire dewatering uses blades downstream of the forming roll arranged to support the wires and dewater the remaining fibre suspension through the first and second wires. In such apparatuses initial dewatering of the fibre suspension takes place over the forming roll.
- the wires witch the fibre webs and intermediate, remaining un-dewatered fibre suspension are then removed from the forming roll and lead to the subsequent blade arrangement, where dewatering is generated by pressure pulses.
- dewatering is generated by pressure pulses.
- local under pressures will be generated at closed areas in the surface of the forming roll. These local under pressures correspond to the suction pulses generated in the table roll dewatering in the fourdrinier dewatering arrangement discussed above.
- the local under pressures will deflect the first wire and the fibre web positioned thereon towards the roll surface, while the second wire is following an essentially straight path towards the first outer dewatering element following the roll. This results in an expanding space between the wires at the departure from the roll.
- the dewatering pressure at the roll dewatering is nominally T/R, where T is the tensile stress of the second wire and R is the radius of the roll.
- T is the tensile stress of the second wire
- R is the radius of the roll.
- the shortest technically possible length for the first wire from its departure from the forming roll to its reaching the first support blade has so far been of the magnitude of 200 mm.
- One of the aims with the present invention is therefore to provide an arrangement that substantially reduces these unwanted effects.
- An especially advantageous embodiment of the present invention discloses a distance from the separation line to the blade of less than 30 mm.
- a further advantageous embodiment of the present invention discloses a blade where the side of the blade facing the forming roll has a shape corresponding to that of the roll surface.
- a more advantageous embodiment of the present invention discloses a blade where the side of the blade facing the first wire is essentially flat.
- Fig. 1 discloses a part of a twin-wire forming apparatus with a forming roll 1, a first wire 2 partly wrapped directly around the forming roll 1, a second wire 3 wrapped around the forming roll lying on the first wire 2.
- a head box 4 is arranged with its opening directed substantially in the feeding direction of the wires 2, 3.
- the head box feeds stock to the nip between the wires 2, 3 wrapped around the forming roll 1.
- a first support blade 5 is arranged inside of the first wire 2.
- This blade is designed to support the first wire 2 and to avoid under pressure generation between the first wire 2 and the surface of the forming roll 1 by breaking the fluid capillary between the first wire 2 and the forming roll surface. If this happens early on any substantial force will not form from a local under pressure between roll and wire. This means that any substantial deformation of wire 2 leading to sheet damage will be avoided. This means in turn that the tip of the blade 5 will not be exposed to any significant radial force from the inner wire, thus not causing any significant blade wear by friction.
- the blade 5 is thus designed so that it supports the inner wire at a distance of at the most approx. 100 mm, and more preferably approx. 20-30 mm downstream of the separation line on the forming roll surface.
- the blade 5 has for geometrical reasons (the closeness to the roll nip) a very small thickness at its leading edge, of the magnitude of one millimeter, as can be understood from the above equation and from fig. 2 .
- Such a blade gets thereby a low flexural rigidity, and will not be able to carry any significant loads from the inner wire. Therefore the blade 5 is designed so that the inner side has a curvature adjusted to support against the forming roll while the outer side is essentially plane to support the inner wire.
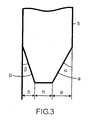
- the blade tip must therefore be designed so that a suitable amount lubricating water is let through between the blade and the roll surface. This is effected by the taper (a, ⁇ ) on the roll side of the tip, see figure 3 . As can be seen from the figure, this taper angle is ⁇ .
- Minimum wear between the wire side of the blade 5 and the first wire 2 is obtained by that a suitable water layer is let through between the wire and the blade 5. This is accomplished by a suitable tapering (b, ⁇ ) of the wire side of the tip of blade 5, see figure 3 . As can be seen from the figure, this taper angle is ⁇ .
- the design of the blade according the invention can, of course, be given different forms within the scope of the claims, and is not limited to the example above.
- the blade may be manufactured from ceramic, polymeric or metallic materials, or combinations thereof. Also other material combinations are possible.
Landscapes
- Paper (AREA)
- Sink And Installation For Waste Water (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Centrifugal Separators (AREA)
Abstract
Description
- The present invention relates to a dewatering apparatus adapted for use in a twin-wire dewatering section of a paper machine. More specifically it relates to an apparatus comprising a rotating forming roll, a head box for supplying stock, arranged before the forming roll, a closed loop first wire, also called inner wire, adapted to be partly wrapped around the forming roll up to a separation line where its contact with the forming roll ceases, and to receive the stock from the head box on its surface not facing the forming roll, a closed loop second wire, also called outer wire, adapted to be partly wrapped around the forming roll on top of the first wire thereby pressing the stock between itself and the first wire, and a first blade substantially parallel to the forming roll, said blade being arranged to support the roll facing side of the first wire after the separation line from the forming roll and being arranged such that the tip of the blade is directed against the wire transporting direction. Such an arrangement is known from
WO-A-96/32533 - One conventional fourdrinier dewatering system for a paper machine comprises table rolls as dewatering elements. The limitations of using table rolls as dewatering elements in fourdrinier wire parts appear at high wire speeds. The local under pressure generated in the outgoing nip between wire bottom and roll surface then becomes too high. This under pressure will generate a local downward movement of the wire, which thereafter has to move back upwards to the top level of the following table roll. The vertical upward movement of the free fibre suspension on top of the wire (and the already dewatered part of the web) will then become so intense that drops form and escape from the suspension surface, which may generate formation disturbances.
- The amplitude of the under pressure pulses generated by the table rolls increases with the square of the wire speed. At wire speeds in excess of approx. 500m/min. the suction pulses will become so intense that the formation deteriorates.
- A further principle of twin-wire dewatering uses blades downstream of the forming roll arranged to support the wires and dewater the remaining fibre suspension through the first and second wires. In such apparatuses initial dewatering of the fibre suspension takes place over the forming roll.
- The wires witch the fibre webs and intermediate, remaining un-dewatered fibre suspension are then removed from the forming roll and lead to the subsequent blade arrangement, where dewatering is generated by pressure pulses. At the separation line of the removal of the wires from the forming roll, local under pressures will be generated at closed areas in the surface of the forming roll. These local under pressures correspond to the suction pulses generated in the table roll dewatering in the fourdrinier dewatering arrangement discussed above.
- The local under pressures will deflect the first wire and the fibre web positioned thereon towards the roll surface, while the second wire is following an essentially straight path towards the first outer dewatering element following the roll. This results in an expanding space between the wires at the departure from the roll.
- The dewatering pressure at the roll dewatering is nominally T/R, where T is the tensile stress of the second wire and R is the radius of the roll. When the two wires leave the roll the dewatering pressure drops down to the atmospheric pressure. This generates an acceleration of the free suspension between the fibre webs. According to the principle of mass conservation this acceleration should be coupled to a decreasing space between the wires.
- The total effect of the two above-mentioned phenomena, i.e. the local increase in wire separation space owing to the under pressure at the departure from the roll simultaneously as the flow velocity increase technically instead would need a local decrease in wire separation, gives rise to different types of disturbances in the remaining fibre suspension, which in turn may result in sheet damages.
- The shortest technically possible length for the first wire from its departure from the forming roll to its reaching the first support blade has so far been of the magnitude of 200 mm.
- This may however result in, as is described above, sheet damages.
- One of the aims with the present invention is therefore to provide an arrangement that substantially reduces these unwanted effects.
- This is obtained in that the distance from the separation line to the blade is less than 100 mm.
- An especially advantageous embodiment of the present invention discloses a distance from the separation line to the blade of less than 30 mm.
- The free wire distance L from roll separation to blade tip obeys the following relationship with the blade tip thickness h and the forming roll diameter D: L = sqrt(h x D).
- A further advantageous embodiment of the present invention discloses a blade where the side of the blade facing the forming roll has a shape corresponding to that of the roll surface.
- A more advantageous embodiment of the present invention discloses a blade where the side of the blade facing the first wire is essentially flat.
- Further advantages with the present invention will be described in fuller detail in the following description of preferred embodiments of the invention with reference to the accompanying drawings.
-
Fig. 1 discloses a fundamental view of an apparatus according to the present invention. -
Fig. 2 discloses a detailed side view of a blade according to the present invention. -
Fig. 3 discloses a side view of a tip of a blade according to the present invention. -
Fig. 1 discloses a part of a twin-wire forming apparatus with a formingroll 1, afirst wire 2 partly wrapped directly around the formingroll 1, asecond wire 3 wrapped around the forming roll lying on thefirst wire 2. Before the formingroll 1 between the twowires wires wires roll 1. By changing the angle of the opening of the head box 4 against this nip it is possible to change the direction of the stock fed to the forming apparatus. - At a distance downstream of the separation line where the wires leave contact with the forming roll surface a
first support blade 5 is arranged inside of thefirst wire 2. This blade is designed to support thefirst wire 2 and to avoid under pressure generation between thefirst wire 2 and the surface of the formingroll 1 by breaking the fluid capillary between thefirst wire 2 and the forming roll surface. If this happens early on any substantial force will not form from a local under pressure between roll and wire. This means that any substantial deformation ofwire 2 leading to sheet damage will be avoided. This means in turn that the tip of theblade 5 will not be exposed to any significant radial force from the inner wire, thus not causing any significant blade wear by friction. - The
blade 5 is thus designed so that it supports the inner wire at a distance of at the most approx. 100 mm, and more preferably approx. 20-30 mm downstream of the separation line on the forming roll surface. Theblade 5 has for geometrical reasons (the closeness to the roll nip) a very small thickness at its leading edge, of the magnitude of one millimeter, as can be understood from the above equation and fromfig. 2 . Such a blade gets thereby a low flexural rigidity, and will not be able to carry any significant loads from the inner wire. Therefore theblade 5 is designed so that the inner side has a curvature adjusted to support against the forming roll while the outer side is essentially plane to support the inner wire. - Referring now to
fig. 3 , by choosing different tapering of the roll and wire side resp. (see a and b resp.) of the tip of the blade the radial force generated by the flow deflections can be controlled. A higher value of the taper on the roll side gives a resulting force to the wire side. - Minimum wear between the roll side of the
blade 5 and the roll surface must be ensured. The blade tip must therefore be designed so that a suitable amount lubricating water is let through between the blade and the roll surface. This is effected by the taper (a, α) on the roll side of the tip, seefigure 3 . As can be seen from the figure, this taper angle is α. - Minimum wear between the wire side of the
blade 5 and thefirst wire 2 is obtained by that a suitable water layer is let through between the wire and theblade 5. This is accomplished by a suitable tapering (b, β) of the wire side of the tip ofblade 5, seefigure 3 . As can be seen from the figure, this taper angle is β. - Downstream of the
first blade 5 other blades can be arranged further supporting and deflecting the wires, thus creating pressure pulses for dewatering of the remaining fibre suspension. - Test runs in the experimental paper machine FEX at STFI-Packforsk have shown that with conventional design the
inner wire 2 may, already at forming speeds of approx. 1200 mlmin, and a suction box vacuum of 10 kPa in the forming roll, separate owing to local under pressures, whereby the free suspension between the wires is redistributed. At a roll surrounding angle of 30° thereby serious formation damages arose. By using the blade according to the invention these damages were completely avoided. - With decreased suspension quantity between the wires, which was obtained from an increase of the wire surrounding angle to 35°, the web structure damages appeared as distinct bands. Also these damages were avoided completely by using a blade according to the invention.
- The design of the blade according the invention can, of course, be given different forms within the scope of the claims, and is not limited to the example above. The blade may be manufactured from ceramic, polymeric or metallic materials, or combinations thereof. Also other material combinations are possible.
Claims (10)
- Dewatering arrangement adapted for use in a twin-wire dewatering section of a paper machine, said arrangement comprising a rotating forming roll (1), a head box (4) for supplying stock arranged before the forming roll (1), a a closed loop first wire (2) adapted to be partly wrapped around the forming roll (1) up to a separation line where its contact with the forming roll (1) ceases, and to receive the stock from the head box (4) on its surface not facing the forming roll (1), a closed loop second wire (3) adapted to be partly wrapped around the forming roll (1) on top of the first wire (2) thereby pressing the stock between itself and the first wire (2), and a first blade (5) substantially parallel to the forming roll (1), said blade (5) being arranged to support the roll facing side of the first wire (2) after the separation line from the forming roll (1) and being arranged such that the tip of the blade (5) is directed against the wire transporting direction, characterized in that the distance from the separation line to the blade (5) is less than 100 mm.
- Dewatering arrangement according to claim 1, where the distance from the separation line to the blade is less than 30 mm.
- Dewatering arrangement according to one of claims 1-2, where the side of the blade facing the forming roll has a shape corresponding to that of the roll surface.
- Dewatering arrangement according to one of claims 1-3, where the side of the blade facing the first wire is essentially flat.
- Dewatering arrangement according to one of claims 1-4, where the tip of the blade on its side facing the forming roll is tapered with an angle α to the longitudinal axis of the blade.
- Dewatering arrangement according to one of claims 1-5, where the tip of the blade on its side facing the first wire is tapered with an angle β to the longitudinal axis of the blade.
- Dewatering arrangement according to one of claims 1-6, where the blade is manufactured of ceramic material.
- Dewatering arrangement according to one of claims 1-6, where the blade is manufactured of polymeric material.
- Dewatering arrangement according to one of claims 1-6, where the blade is manufactured of metallic material.
- Dewatering arrangement according to one of claims 1-6, where the blade is manufactured of a combination of two or more materials of a group comprising ceramic material, polymeric material and metallic material.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SE0500447 | 2005-02-28 | ||
| PCT/SE2006/000256 WO2006091165A1 (en) | 2005-02-28 | 2006-02-27 | Dewatering apparatus |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1853760A1 EP1853760A1 (en) | 2007-11-14 |
| EP1853760B1 true EP1853760B1 (en) | 2008-10-08 |
Family
ID=36927704
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06716944A Expired - Lifetime EP1853760B1 (en) | 2005-02-28 | 2006-02-27 | Dewatering apparatus |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1853760B1 (en) |
| AT (1) | ATE410544T1 (en) |
| DE (1) | DE602006003070D1 (en) |
| WO (1) | WO2006091165A1 (en) |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3232825A (en) * | 1963-09-16 | 1966-02-01 | Time Inc | Dual wire type paper-forming apparatus and methods of forming and dewatering paper |
| US4875977A (en) * | 1987-04-17 | 1989-10-24 | The Black Clawson Company | Horizontal twin wire machine with vertically adjustable open roll and deflector blade |
| ATE386155T1 (en) * | 2002-09-13 | 2008-03-15 | Voith Patent Gmbh | DOUBLE SCREEN FORMER FOR PRODUCING A FIBROUS WEB |
-
2006
- 2006-02-27 WO PCT/SE2006/000256 patent/WO2006091165A1/en not_active Ceased
- 2006-02-27 AT AT06716944T patent/ATE410544T1/en not_active IP Right Cessation
- 2006-02-27 EP EP06716944A patent/EP1853760B1/en not_active Expired - Lifetime
- 2006-02-27 DE DE602006003070T patent/DE602006003070D1/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE602006003070D1 (en) | 2008-11-20 |
| ATE410544T1 (en) | 2008-10-15 |
| EP1853760A1 (en) | 2007-11-14 |
| WO2006091165A1 (en) | 2006-08-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| NO823469L (en) | FAST DRYING OF PAPER. | |
| US3056719A (en) | Continuous web forming machine | |
| FI84734B (en) | DOUBLE VAPOR FORM PAPER MACHINE. | |
| JP2005536654A (en) | Formation of paper or paperboard web in twin wire former or twin wire section of former | |
| WO1982002938A1 (en) | A vacuum box for use in high speed papermaking | |
| US4300714A (en) | Method and apparatus for silencing of webs | |
| KR100423180B1 (en) | Roll and blade twin-wire gap former for a paper machine | |
| EP2697424B1 (en) | A suction roll and a method of operating such a suction roll | |
| US20020108732A1 (en) | Twin wire former for the production of a fiber web from a fiber suspension | |
| US5427654A (en) | Multi-ply web forming apparatus | |
| US6454903B2 (en) | Method and apparatus for the transfer of a lead strip of a paper web | |
| US3432385A (en) | Water extraction devices | |
| EP1853760A1 (en) | Dewatering apparatus | |
| US6502434B1 (en) | Effluent shower for pulp washer | |
| SE501332C2 (en) | Ways to form a tissue paper web | |
| EP1853759B1 (en) | Dewatering arrangement adapted for use in a twin-wire dewatering section of a stock processing machine | |
| EP1740766B1 (en) | Apparatus and method for a paper machine | |
| US20060186235A1 (en) | Method for refining paper or cellulose fibers in an aqueous suspension | |
| US20070235152A1 (en) | On-machine coater | |
| US6592715B2 (en) | Device for the production of a multi-layer fiber stock web | |
| EP1270806B1 (en) | Headbox with rotating side walls | |
| US3623945A (en) | Wire-mounting arrangement on a twin-wire vertical papermaking machine | |
| JP5032845B2 (en) | Winding method for paper, paperboard or raw web and winder for paper, paperboard or raw web | |
| CA1256730A (en) | Web forming device | |
| EP1315861A1 (en) | Grooved lead blade for a papermaking machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20070816 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 602006003070 Country of ref document: DE Date of ref document: 20081120 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090119 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090108 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20090211 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090218 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090208 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| 26N | No opposition filed |
Effective date: 20090709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090228 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20091030 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090302 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20100215 Year of fee payment: 5 Ref country code: IT Payment date: 20100220 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20100312 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090109 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100228 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20100212 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081008 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110227 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110227 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602006003070 Country of ref document: DE Effective date: 20110901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110901 |