EP1418829B1 - Method for manufacturing a beam for a storage rack and arrangement for beams for storage racks - Google Patents
Method for manufacturing a beam for a storage rack and arrangement for beams for storage racks Download PDFInfo
- Publication number
- EP1418829B1 EP1418829B1 EP02720241A EP02720241A EP1418829B1 EP 1418829 B1 EP1418829 B1 EP 1418829B1 EP 02720241 A EP02720241 A EP 02720241A EP 02720241 A EP02720241 A EP 02720241A EP 1418829 B1 EP1418829 B1 EP 1418829B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- section
- pressed
- holes
- flat
- plane surface
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 12
- 238000003860 storage Methods 0.000 title claims description 11
- 238000004519 manufacturing process Methods 0.000 title claims description 6
- 239000000463 material Substances 0.000 claims description 18
- 238000005304 joining Methods 0.000 description 5
- 238000003825 pressing Methods 0.000 description 3
- 238000003466 welding Methods 0.000 description 3
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 238000005452 bending Methods 0.000 description 1
- 210000000078 claw Anatomy 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 230000000717 retained effect Effects 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
- 229910052725 zinc Inorganic materials 0.000 description 1
Images
Classifications
-
- A—HUMAN NECESSITIES
- A47—FURNITURE; DOMESTIC ARTICLES OR APPLIANCES; COFFEE MILLS; SPICE MILLS; SUCTION CLEANERS IN GENERAL
- A47B—TABLES; DESKS; OFFICE FURNITURE; CABINETS; DRAWERS; GENERAL DETAILS OF FURNITURE
- A47B96/00—Details of cabinets, racks or shelf units not covered by a single one of groups A47B43/00 - A47B95/00; General details of furniture
- A47B96/14—Bars, uprights, struts, or like supports, for cabinets, brackets, or the like
- A47B96/1441—Horizontal struts
-
- A—HUMAN NECESSITIES
- A47—FURNITURE; DOMESTIC ARTICLES OR APPLIANCES; COFFEE MILLS; SPICE MILLS; SUCTION CLEANERS IN GENERAL
- A47B—TABLES; DESKS; OFFICE FURNITURE; CABINETS; DRAWERS; GENERAL DETAILS OF FURNITURE
- A47B57/00—Cabinets, racks or shelf units, characterised by features for adjusting shelves or partitions
- A47B57/30—Cabinets, racks or shelf units, characterised by features for adjusting shelves or partitions with means for adjusting the height of detachable shelf supports
- A47B57/40—Cabinets, racks or shelf units, characterised by features for adjusting shelves or partitions with means for adjusting the height of detachable shelf supports consisting of hooks coacting with openings
- A47B57/402—Hooks attached to a member embracing at least two sides of an upright, e.g. an angle bracket
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D39/00—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders
- B21D39/03—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders of sheet metal otherwise than by folding
- B21D39/031—Joining superposed plates by locally deforming without slitting or piercing
Definitions
- the invention relates to a method for manufacturing a beam for a storage rack, in which method a profiled beam of suitable cross-section is pressed together or pressed flat at both ends and hooks are provided there for engagement with holes in uprights in the storage rack which are provided with rows of holes.
- the invention also relates to an arrangement for beams for storage racks, which beams are designed to be fastened to uprights provided with rows of holes, each beam consisting of a section of suitable cross-section, the two ends of which are pressed together to form a plane surface in each case, which extends in the longitudinal direction of the beam, which plane surface is connected to a, preferably angle, section with hooks, bent out from the side connected to the plane surface, for engagement with holes in said rows of holes.
- a similar arrangement for beams is already known by US-A- 3 647 079.
- a supporting beam which, together with a corresponding, parallel supporting beam, constitutes a horizontal "shelf" on which the pallets can rest.
- a supporting beam usually consists of three parts, namely a beam section of a given length and a fitting (end attachment/locking piece) at each end of the beam.
- Said fittings are equipped with a form of hook/lip for fixing into corresponding holes in vertical frames/uprights.
- the fittings are normally joined to the beam sections by welding.
- a disadvantage of this is that the weld has to be lacquered or painted afterwards, which involves a considerable production cost.
- it particularly advantageous to use galvanized sections and end attachments because the welding destroys the thin zinc layer, so that the weld is susceptible to corrosion. The weld thus needs to be lacquered or painted afterwards, which increases the production costs of supporting beams.
- Another embodiment of supporting beams in pallet racks is one where the supporting beam is made in one piece and the section itself of the supporting beams is flattened at each end and hooks are formed directly in the flattened section material.
- a disadvantage of such an embodiment is that it is then necessary to have the same material thickness and quality in both the beam section itself and the end attachments, with the result that, by optimizing the material in the beam section itself, that is, to use the minimum amount of material to give the desired load bearing capacity, too little strength is obtained in the end attachments, or that, by optimizing with regard to the end attachments, the material consumption in the beam section is excessive and uneconomical.
- the present invention relates to pallet racks in which the supporting beams consist of a number of parts, that is to say the beam section itself and the associated fittings.
- the advantage of this is that it is possible to select different thickness and qualities for the fittings or end attachments in relation to the beam section itself.
- each of the pressed-flat ends is brought into contact with an end section, which end section is provided with hooks for engagement with the holes in the uprights, and in that the pressed-flat beam end and said end section are interconnected by discrete material portions, which form rivets, being pressed through the pressed-flat beam end from the angle side.
- an arrangement as mentioned in the introduction is also proposed, which arrangement is characterized in that the plane surface and said end section are in mutual contact and are interconnected by discrete material portions, which form rivets, pressed through the plane surface from the angle side.
- the pressed-together or pressed-flat beam portions are located at the two beam ends, but it is also possible to imagine beam embodiments in which one or more pressed-flat or pressed-together beam portion(s) is or are present between the two beam ends, which beam portion or beam portions is or are provided with one or two end sections as mentioned, if appropriate a U section with hooks bent out in the U bottom.
- the joining technique employed is a "riveting" technique which can be performed by a pressing tool being introduced partly into the two plates which have been placed together and pressing out a discrete material portion in such a manner that a type of rivet connection is formed.
- the invention results in the production costs of pallet racks being reduced considerably, especially when compared with welded and lacquered solutions.
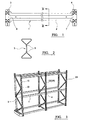
- the supporting beam 1 shown in Fig. 1 consists of three components, namely a beam section 2 and an end section for each end, the end sections being in the form of angle sections 3 and 4 having in cross-section two arms substantially at right angles to each other.
- the beam section 2 has a cross-sectional shape known per se as shown in Fig. 2, and the beam section is shaped like this by bending a plate into the shape shown in Fig. 2.
- Alternative cross-sections may be provided to suit required sizes and load capacities.
- Reference number 5 indicates suitable connections made by a joining technique as described hereinafter with reference to Fig. 9.
- the beam section 2 is pressed flat at each end, that is to say it is designed with a pressed-together portion 6, 7 in such a manner that, at each end of the supporting beam 1, a plane surface is formed, which extends in the longitudinal direction of the beam.
- the rows of holes in the uprights 10 are not shown in greater detail, however, as this technique is well known to the person skilled in the art.
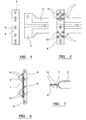
- the angle side 8 provided with the hooks or the claws 9 is placed against the pressed-together beam end portion 7 and is connected thereto by discrete material portions 11, which will go into and through the plane surface 7 and each form a rivet connection, being pressed out from the angle side 8, more specifically from that side thereof where the hooks 9 are pressed out.
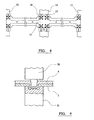
- FIG. 9 shows a section through a typical "rivet" connection known per se which can be used.
- the angle side 8 bears against the pressed-together beam end portion 7.
- a pressing tool 20 presses the material of the angle 8 and of the end portion 7 against a female reaction member 21, by means of which a rivet connection as shown is formed.
- the individual beams 1 will be made as shown in Fig. 1, but it is also possible to imagine supporting beam embodiments in which pressed-flat portions are designed between the ends provided with fastening fittings, at which portions fittings are mounted, so that therefore, as shown in Fig. 8 for example, a supporting beam 1' can extend over and past an upright 14 arranged between two uprights 12, 13. Angle sections 16, 17 are then, like at the beam ends, fixed into the intermediate pressed-flat portion 15. If appropriate, the two angle sections 16, 17 can be designed as an integrated unit, and also as a U section. Beam embodiments such as that shown in Fig. 8 can suitably be used to produce a storage rack which is better held together and more stable, so that, for example, the storage rack shown in Fig. 3 then has longitudinal beams which thus extend from the upright 12 to the upright 18 in Fig. 3.
- the advantages mentioned in the introduction are achieved by means of the invention.
- the individual elements can be treated in advance, for example galvanized or lacquered.
- the use of angle sections in the end fittings also provides increased stability in the storage rack.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Assembled Shelves (AREA)
- Connection Of Plates (AREA)
- Particle Accelerators (AREA)
Description
- The invention relates to a method for manufacturing a beam for a storage rack, in which method a profiled beam of suitable cross-section is pressed together or pressed flat at both ends and hooks are provided there for engagement with holes in uprights in the storage rack which are provided with rows of holes.
- The invention also relates to an arrangement for beams for storage racks, which beams are designed to be fastened to uprights provided with rows of holes, each beam consisting of a section of suitable cross-section, the two ends of which are pressed together to form a plane surface in each case, which extends in the longitudinal direction of the beam, which plane surface is connected to a, preferably angle, section with hooks, bent out from the side connected to the plane surface, for engagement with holes in said rows of holes. A similar arrangement for beams is already known by US-A- 3 647 079.
- One of the main components of a pallet rack system is a supporting beam which, together with a corresponding, parallel supporting beam, constitutes a horizontal "shelf" on which the pallets can rest. Such a supporting beam usually consists of three parts, namely a beam section of a given length and a fitting (end attachment/locking piece) at each end of the beam. Said fittings are equipped with a form of hook/lip for fixing into corresponding holes in vertical frames/uprights. The fittings are normally joined to the beam sections by welding. A disadvantage of this is that the weld has to be lacquered or painted afterwards, which involves a considerable production cost. Nor is it particularly advantageous to use galvanized sections and end attachments, because the welding destroys the thin zinc layer, so that the weld is susceptible to corrosion. The weld thus needs to be lacquered or painted afterwards, which increases the production costs of supporting beams.
- Another embodiment of supporting beams in pallet racks is one where the supporting beam is made in one piece and the section itself of the supporting beams is flattened at each end and hooks are formed directly in the flattened section material. A disadvantage of such an embodiment is that it is then necessary to have the same material thickness and quality in both the beam section itself and the end attachments, with the result that, by optimizing the material in the beam section itself, that is, to use the minimum amount of material to give the desired load bearing capacity, too little strength is obtained in the end attachments, or that, by optimizing with regard to the end attachments, the material consumption in the beam section is excessive and uneconomical.
- The present invention relates to pallet racks in which the supporting beams consist of a number of parts, that is to say the beam section itself and the associated fittings. The advantage of this is that it is possible to select different thickness and qualities for the fittings or end attachments in relation to the beam section itself.
- It is a particular aim of the invention to make it possible to use materials which are surface-treated in advance, for example pre-lacquered/painted or pre-galvanized materials, for both the beam section and the fittings.
- It is a particular aim to use a joining technique which provides the desired load capacity and load rigidity in the connection between the beam sections and the end attachments and between the end attachments and the uprights.
- According to the invention, a method as mentioned in the introduction is therefore proposed, which is characterized in that each of the pressed-flat ends is brought into contact with an end section, which end section is provided with hooks for engagement with the holes in the uprights, and in that the pressed-flat beam end and said end section are interconnected by discrete material portions, which form rivets, being pressed through the pressed-flat beam end from the angle side.
- According to the invention, an arrangement as mentioned in the introduction is also proposed, which arrangement is characterized in that the plane surface and said end section are in mutual contact and are interconnected by discrete material portions, which form rivets, pressed through the plane surface from the angle side.
- The pressed-together or pressed-flat beam portions are located at the two beam ends, but it is also possible to imagine beam embodiments in which one or more pressed-flat or pressed-together beam portion(s) is or are present between the two beam ends, which beam portion or beam portions is or are provided with one or two end sections as mentioned, if appropriate a U section with hooks bent out in the U bottom.
- It will be understood that what distinguishes the invention is that the components are joined together mechanically without the use of heat (welding) or any form of additional material/components. In this way, the advantage is obtained of being able to select different thicknesses and qualities for the end attachments in relation to the beam section itself, and possibilities are afforded for using materials which are surface-treated in advance. A considerable advantage in this connection is an environmental advantage which is obtained by avoiding the heating/melting of the materials.
- The joining technique employed is a "riveting" technique which can be performed by a pressing tool being introduced partly into the two plates which have been placed together and pressing out a discrete material portion in such a manner that a type of rivet connection is formed.
- By virtue of the pressing-out of the material taking place from the end sections where the bent-out hooks are pressed out, the surface, which is otherwise smooth there and is designed for contact with the respective upright, is retained.
- The invention results in the production costs of pallet racks being reduced considerably, especially when compared with welded and lacquered solutions.
- The invention will now be explained in greater detail with reference to the drawings, in which:-
- Fig. 1
- shows a front view of a supporting beam according to the invention;
- Fig. 2
- shows a section through the supporting beam in Fig. 1 along section line II;
- Fig. 3
- shows an example of a pallet rack with supporting beams according to the invention;
- Fig. 4
- shows a pressed-flat beam section end and an angle section before joining together;
- Fig. 5
- shows the two components shown in Fig. 4 joined together;
- Fig. 6
- shows an end view of the supporting beam in Figs 1 and 5;
- Fig. 7
- shows a top view of the end detail in Fig. 5;
- Fig. 8
- shows a front view of a possible beam embodiment according to the invention, and
- Fig. 9
- shows a section through a typical "rivet" connection.
- The supporting
beam 1 shown in Fig. 1 consists of three components, namely abeam section 2 and an end section for each end, the end sections being in the form ofangle sections - The
beam section 2 has a cross-sectional shape known per se as shown in Fig. 2, and the beam section is shaped like this by bending a plate into the shape shown in Fig. 2. Alternative cross-sections may be provided to suit required sizes and load capacities.Reference number 5 indicates suitable connections made by a joining technique as described hereinafter with reference to Fig. 9. - The
beam section 2 is pressed flat at each end, that is to say it is designed with a pressed-together portion beam 1, a plane surface is formed, which extends in the longitudinal direction of the beam. - Each
angle section angle section 4 in Figs 4 to 7, is provided on oneangle side 8 with a number of pressed-outhooks 9, designed to be hung in a manner known per se in holes in rows of holes inuprights 10 in a pallet rack, see Fig. 3. In Fig. 3, the rows of holes in theuprights 10 are not shown in greater detail, however, as this technique is well known to the person skilled in the art. - The
angle side 8 provided with the hooks or theclaws 9 is placed against the pressed-togetherbeam end portion 7 and is connected thereto by discretematerial portions 11, which will go into and through theplane surface 7 and each form a rivet connection, being pressed out from theangle side 8, more specifically from that side thereof where thehooks 9 are pressed out. - This joining technique is known. Fig. 9 shows a section through a typical "rivet" connection known per se which can be used. The
angle side 8 bears against the pressed-togetherbeam end portion 7. Apressing tool 20 presses the material of theangle 8 and of theend portion 7 against afemale reaction member 21, by means of which a rivet connection as shown is formed. - In most cases, the
individual beams 1 will be made as shown in Fig. 1, but it is also possible to imagine supporting beam embodiments in which pressed-flat portions are designed between the ends provided with fastening fittings, at which portions fittings are mounted, so that therefore, as shown in Fig. 8 for example, a supporting beam 1' can extend over and past an upright 14 arranged between twouprights Angle sections flat portion 15. If appropriate, the twoangle sections - The advantages mentioned in the introduction are achieved by means of the invention. The individual elements can be treated in advance, for example galvanized or lacquered. The use of angle sections in the end fittings also provides increased stability in the storage rack.
Claims (5)
- Method for manufacturing a supporting beam (1) for a storage rack, in which method a beam section (2) of suitable cross-section is pressed flat (6, 7) at both ends and hooks (9) are provided there for engagement with holes in uprights (10, 13) in the storage rack which are provided with rows of holes, characterized in that each such pressed-flat end (6, 7) is brought into contact with an end-section (8) which end section (8) is provided with hooks (9) for engagement with said holes, and in that the pressed-flat beam end (7) and said end section (8) are interconnected by discrete material portions (11), which form rivets, being pressed through the pressed-flat beam end (7) from the angle side (8).
- Arrangement for supporting beams (1) for storage racks, which beams (1) are designed to be fastened to uprights (10, 13) provided with rows of holes, each beam (1) consisting of a beam section (2) of suitable cross-section, the two ends of which are pressed together to form a plane surface (6, 7) in each case, which extends in the longitudinal direction of the beam, which plane surface (7) is connected to an end section (8) with hooks (9), formed out from the end section connected to the plane surface (7), for engagement with holes in said rows of holes, characterized in that the plane surface (7) and said end section (8) are in mutual contact and are interconnected by discrete material portions (11), which form rivets, pressed through the plane surface (7) from the end section (8).
- Arrangement according to Claim 2, characterized by one or more pressed-flat beam portions (15) between the two beam ends, which beam portion (15) is provided with one or two mid-sections (16, 17).
- Arrangement according to Claim 3, wherein the mid-sections have a U-shaped cross-section with hooks formed out in the U bottom.
- Arrangement according to Claims 2, 3 or 4, wherein the end sections comprise an angle section (4).
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| NO20013930 | 2001-08-13 | ||
| NO20013930A NO313264B1 (en) | 2001-08-13 | 2001-08-13 | Method of manufacturing a beam for a storage rack and arrangement of beams for storage rack |
| PCT/GB2002/001828 WO2003015579A1 (en) | 2001-08-13 | 2002-04-19 | Method for manufacturing a beam for a storage rack and arrangement for beams for storage racks |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1418829A1 EP1418829A1 (en) | 2004-05-19 |
| EP1418829B1 true EP1418829B1 (en) | 2007-01-17 |
| EP1418829B8 EP1418829B8 (en) | 2007-04-25 |
Family
ID=19912728
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02720241A Expired - Lifetime EP1418829B8 (en) | 2001-08-13 | 2002-04-19 | Method for manufacturing a beam for a storage rack and arrangement for beams for storage racks |
Country Status (6)
| Country | Link |
|---|---|
| EP (1) | EP1418829B8 (en) |
| DE (1) | DE60217682D1 (en) |
| DK (1) | DK1418829T3 (en) |
| NO (1) | NO313264B1 (en) |
| PL (1) | PL197715B1 (en) |
| WO (1) | WO2003015579A1 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT202300023292A1 (en) * | 2023-11-06 | 2025-05-06 | Rosss S P A | WAREHOUSE WITH IMPROVED TRANSPORTABILITY |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ES2212717B1 (en) * | 2002-05-20 | 2006-02-16 | Carpinteria Metalica Bengolea, S.L. | HOLDING DEVICE FOR BAKERY TRAYS. |
| DE102006021148B4 (en) * | 2006-05-06 | 2014-03-27 | Schaeffler Technologies Gmbh & Co. Kg | Connection of sheet metal components of a gearbox |
| DE502008003275D1 (en) * | 2007-02-13 | 2011-06-01 | Inventio Ag | METHOD OF CLAMPING THICK METAL WORKPIECES AND USE OF A CLINCH TOOL |
| GB2508789A (en) * | 2009-11-27 | 2014-06-18 | Ivan Glenfield Quail | Near-rigid beam to column connector system |
| CN103464585B (en) * | 2013-08-01 | 2015-05-27 | 浙江利帆家具有限公司 | Lower stamping mould for round-pipe supporting piece |
| US11700937B2 (en) | 2020-09-08 | 2023-07-18 | Grillnetics LLC | Enclosure assembly system |
| IT202100004181A1 (en) * | 2021-02-23 | 2022-08-23 | Andrea Cammi | CURRENT FOR SHELVING AND PROCEDURE FOR ITS REALIZATION |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SE325527B (en) * | 1969-05-09 | 1970-06-29 | Electrolux Ab | |
| US5036778A (en) * | 1990-03-21 | 1991-08-06 | Antonello Briosi | Assemblable modular elements, in particular in thin sheet, for the formation of a metal shelving |
| US5432989A (en) * | 1992-10-27 | 1995-07-18 | Archer Manufacturing Corporation | Apparatus and method for joining sheet material |
| IT1269074B (en) * | 1994-01-20 | 1997-03-21 | Rosss Dei F Lli Bettini S N C | A TUBULAR PROFILE CROSS FOR THE CONNECTION OF THE UPRIGHTS IN METAL SHELVING |
-
2001
- 2001-08-13 NO NO20013930A patent/NO313264B1/en not_active IP Right Cessation
-
2002
- 2002-04-19 WO PCT/GB2002/001828 patent/WO2003015579A1/en not_active Ceased
- 2002-04-19 PL PL368077A patent/PL197715B1/en not_active IP Right Cessation
- 2002-04-19 DK DK02720241T patent/DK1418829T3/en active
- 2002-04-19 DE DE60217682T patent/DE60217682D1/en not_active Expired - Lifetime
- 2002-04-19 EP EP02720241A patent/EP1418829B8/en not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT202300023292A1 (en) * | 2023-11-06 | 2025-05-06 | Rosss S P A | WAREHOUSE WITH IMPROVED TRANSPORTABILITY |
Also Published As
| Publication number | Publication date |
|---|---|
| PL368077A1 (en) | 2005-03-21 |
| EP1418829A1 (en) | 2004-05-19 |
| NO20013930D0 (en) | 2001-08-13 |
| DK1418829T3 (en) | 2007-05-07 |
| DE60217682D1 (en) | 2007-03-08 |
| PL197715B1 (en) | 2008-04-30 |
| NO20013930A (en) | 2002-09-09 |
| EP1418829B8 (en) | 2007-04-25 |
| NO313264B1 (en) | 2002-09-09 |
| WO2003015579A1 (en) | 2003-02-27 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7258246B2 (en) | Baking tray | |
| US8919585B2 (en) | Decking member | |
| US6094877A (en) | Frame support assembly and method for curved walls | |
| US6055788A (en) | Longitudinal frame support for a commercial vehicle and process for producing the same | |
| WO2003015579A1 (en) | Method for manufacturing a beam for a storage rack and arrangement for beams for storage racks | |
| US11612245B2 (en) | Press-locked grating | |
| GB2205624A (en) | Structural frame components | |
| CA2965058A1 (en) | Rack, load carrier and method of production | |
| US20090308290A1 (en) | Shelf | |
| EP2118546B1 (en) | Bracket for cable ladder and method for the manufacture thereof | |
| KR20100109057A (en) | Insert for fitting rung of cable tray and method of manufacturing the same | |
| KR20100093163A (en) | Insert for fitting rung and cable tray for using the same | |
| JP6583919B2 (en) | Tight frame for folding plate roof construction | |
| DK3307653T3 (en) | Grate, especially for use as shelf for pallet racks or racks for heavy loads | |
| KR101958153B1 (en) | Rung for cable tray and cable tray comprising the rung | |
| EP0855157A1 (en) | Modular structure for metal shelving or the like | |
| KR102046242B1 (en) | Rung joint structure of cable tray | |
| WO2016056912A1 (en) | Composite shelf for a rolling container, rolling container provided therewith and method therefor | |
| JP3646846B2 (en) | Shelf board | |
| KR100958315B1 (en) | Connecting structure of two support | |
| JP2565832B2 (en) | Metal plate thatched roof structure and fasteners for roof plate joints | |
| US20120031866A1 (en) | Decking Member | |
| EP1431475A2 (en) | Bearing element made of cold-rolled or extruded steel section and welded for forming modular structures such as scaffoldings and the like | |
| JP2509436Y2 (en) | Origami roof support structure | |
| CN210095562U (en) | Metal bathroom cabinet frame connecting component and bathroom cabinet |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20040315 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: DE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60217682 Country of ref document: DE Date of ref document: 20070308 Kind code of ref document: P |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: CORK OAK HOLDING LIMITED |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070428 |
|
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: CORK OAK HOLDING LIMITED Effective date: 20070314 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070618 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20070117 |
|
| NLT1 | Nl: modifications of names registered in virtue of documents presented to the patent office pursuant to art. 16 a, paragraph 1 |
Owner name: AKER MATERIAL HANDLING LIMITED Owner name: CORK OAK HOLDING LIMITED |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20071018 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| NLS | Nl: assignments of ep-patents |
Owner name: AKER MATERIAL HANDLING AS Effective date: 20080214 |
|
| NLT1 | Nl: modifications of names registered in virtue of documents presented to the patent office pursuant to art. 16 a, paragraph 1 |
Owner name: CORK OAK HOLDING LIMITED |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070907 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070418 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070419 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070419 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20130410 Year of fee payment: 12 Ref country code: SE Payment date: 20130412 Year of fee payment: 12 Ref country code: GB Payment date: 20130417 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20130410 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP Effective date: 20140430 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20141101 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20140419 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140419 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140420 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140430 |