EP1360134B1 - Method of forming a package from a strip of material - Google Patents
Method of forming a package from a strip of material Download PDFInfo
- Publication number
- EP1360134B1 EP1360134B1 EP01909139A EP01909139A EP1360134B1 EP 1360134 B1 EP1360134 B1 EP 1360134B1 EP 01909139 A EP01909139 A EP 01909139A EP 01909139 A EP01909139 A EP 01909139A EP 1360134 B1 EP1360134 B1 EP 1360134B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- strip
- stack
- package
- stacks
- fold lines
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 26
- 239000000463 material Substances 0.000 title claims description 22
- 230000006835 compression Effects 0.000 claims description 10
- 238000007906 compression Methods 0.000 claims description 10
- 239000005021 flexible packaging material Substances 0.000 claims description 5
- 239000005022 packaging material Substances 0.000 claims description 4
- 238000007789 sealing Methods 0.000 claims 1
- 230000000694 effects Effects 0.000 description 8
- 238000004519 manufacturing process Methods 0.000 description 8
- 239000002699 waste material Substances 0.000 description 7
- 239000000047 product Substances 0.000 description 6
- 230000033001 locomotion Effects 0.000 description 5
- 239000012467 final product Substances 0.000 description 3
- 238000004806 packaging method and process Methods 0.000 description 3
- 230000002745 absorbent Effects 0.000 description 2
- 239000002250 absorbent Substances 0.000 description 2
- 238000007493 shaping process Methods 0.000 description 2
- 150000001875 compounds Chemical class 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 239000004744 fabric Substances 0.000 description 1
- 230000002452 interceptive effect Effects 0.000 description 1
- 239000003550 marker Substances 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 238000004064 recycling Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 238000009461 vacuum packaging Methods 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H35/00—Delivering articles from cutting or line-perforating machines; Article or web delivery apparatus incorporating cutting or line-perforating devices, e.g. adhesive tape dispensers
- B65H35/02—Delivering articles from cutting or line-perforating machines; Article or web delivery apparatus incorporating cutting or line-perforating devices, e.g. adhesive tape dispensers from or with longitudinal slitters or perforators
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/42—Piling, depiling, handling piles
- B65H2301/421—Forming a pile
- B65H2301/4216—Forming a pile of web folded in zig-zag form
- B65H2301/42162—Juxtaposing several piles
Definitions
- Strips of material are used for manufacture of diapers and other absorbent products.
- the strips are cut on the manufacturing line at longitudinally spaced transverse cut lines to divide the strip into individual sheet elements each used in the manufacture of a respective absorbent product.
- these strips are also die cut to provide different widths for shaping of the products to better match the body of the user and for better aesthetics.
- Most current processes of this type die cut the elements from a single strip of the material having a width at least equal to the maximum required width and discard the waste at the sides formed by cutting away the side portions to the narrower scalloped width. Attempts are made to recycle the waste portions, generally by grinding and returning the materials to the strip manufacturer.
- recent developments have increased the complexity of the materials thus increasing the cost and making recycling more difficult. There is therefore pressure to reduce the amount of waste.
- Previously packages of a continuous strip of material have been formed using a technique known as "festooning" in which the strip is folded back and forth to lay a series of strip portions back and forth with each portion being folded relative to the next about a line transverse to the strip.
- the technique of festooning has been available for many years and is used in packaging many different types of materials but particularly material of a fibrous nature such as fabric, non-woven strips and the like.
- the strip is conventionally guided into a receptacle such as a cardboard box while a first reciprocating movement causes portions of the strip to be laid across the receptacle and folded back and forth and a second reciprocating movement causes the positions of the portions to be traversed relative to the receptacle transversely to the portions.
- the receptacle comprises a rigid rectangular container at least partly of cardboard having a base and four upstanding sides.
- Festooning can be used for packaging the strips of varying width but this technique has significant disadvantages which inhibit the effectiveness of the product when removed and processed.
- the fold lines which are essential to the process will interfere with the absorbency or other performance of the material when such fold lines occur at a central area of the sheet element.
- US-A-5,956,926 discloses a method according to the preamble of claim 1.
- the package comprises a generally rectangular body 10 formed from a strip 11 of a material to be packaged and generally this material will be of a fibrous nature formed by woven or non-woven material although this is not essential to the package structure.
- Many materials of various thicknesses can be packaged using the festooning technique provided they can accept the creasing necessary at the end of each portion.
- the package body is formed of a plurality of side by side stacks of the strip where each stack comprises a plurality of folded strip portions of the strip which are laid on top of one another.
- each stack comprises a plurality of folded strip portions of the strip which are laid on top of one another.
- the portions are folded back and forth at respective end fold lines 25 and 26 so that the fold lines lie in a common vertical plane defining the ends 15 and 16 of the stack.
- Each portion of the strip lies directly on top of the previous portion so that side edges 27 and 28 of the portions of the strip define a first set of lines in the common plane at right angles to the strip portions which contain all the side edges 27 of the stack and similarly, the side edges 28 of the strips of the stacks define a second set of lines in the common plane at right angles to the strip portions which contain all the side edges 28 of the stack.
- the package is formed by stacking the portions each on top of the next from a bottom portion 29 up to a top portion 30 to form the stack.
- the package is thus formed from the plurality of stacks 12 each of which has a length equal to that of the other stacks and therefore equal to that of the package and the stacks are formed up to a common height which is therefore equal to the height of the package.
- the package 10 is formed from a plurality of individual stacks 12 arranged side by side. In figure 1 there are shown only three such stacks for convenience of illustration whereas in figure 2 there are shown six such stacks arranged side by side forming a complete package structure. Each stack is formed from a folded strip which is continuous through the stack. Each stack has a top end 13, a bottom end 14, two ends 15 and 16 which are opposed and two sides 17 and 18 which are opposed.
- the dimensions of the package can be varied in according to the requirements so that the number of stacks can be increased or decreased, the length and height of each stack can be varied to increase the number of folded strip portions and to increase the length of the folded strip portions.
- the strips of each stack are folded back and forth from the fold lines 25 to the fold lines 26 to form a folded strip portion having a length equal to the distance between the fold lines.
- the strips are cut so that they have a varying width between the side edges 27 and 28 of the strip.
- the strips are of a simple form in which the width varies periodically between narrow sections 32 and wider sections 33. More complex width variations can be employed in other examples.
- the strip is intended for manufacturing diapers or similar products which are formed each from a respective sheet element cut from the length of the strip.
- Each sheet element in the example shown has an intended cut line 34 at the wider section 33 and a second intended cut line 35 also at the wider section 33 so that the narrower section 32 is located between the intended cut lines.
- the strip has a varying characteristic along its length which determines the position of the sheet elements on the strip and therefore determines the positions of the intended cut lines.
- the varying characteristic is the varying width. Other characteristics such as additional materials or varying thickness can be used.
- each folded strip portion of each of the package bodies is defined by an exact whole number of sheet elements.
- the number of sheet elements is three but this can of course be varied from a minimum of one up to a maximum which depends solely upon to maximum allowable size of the transportable package structure.
- the folded strip portion will contain more than one sheet element since the sheet elements are often of the order of six inches (15.2cm) to two feet (61 cm) in length and the required package structure will be generally significantly larger than this and certainly of the order of four feet (122 cm) in length.
- the design of the wider and narrower portions of the strip is arranged such that no waste is formed when the slitting action occurs and the wider portions match exactly with the narrower portions of the next strips.
- the wider portions of one strip and the narrower portions of the next adjacent strip so that some waste pieces will be formed by cutting out of the structure and discarding of those waste pieces.
- the strip portions will nest each exactly along side the next with the narrower portions of one receiving the wider portions of the next.
- the wider portions do not exactly match the narrower portions, there will still be some nesting effect even though there may be spaces left between the folded strip portions.
- each folded strip portion contains an exact whole number of sheet elements ensures that the cut lines occur directly at the fold lines. Thus there are no fold lines across the strip in any part of the sheet elements after the sheet elements are cut along the cut lines. This is desirable in that the absence of fold lines in the material of the sheet elements will avoid compromising the performance or absorbency of the sheet element in the main body of the sheet element.
- the folded strip portion contains a whole number of the sheet elements and the sheet elements are identical ensures that the side edges of the each folded strip portion lie directly on top of the side edges of the previously laid folded strip portions. There are no overhanging or feathered edge portions therefore and all parts of the strip are fully contained within the stack.
- the stack is therefore in effect a solid structure having a constant density across its width. When compressed therefore the stack can form a very rigid structure with no possibility of damaging the side edges of the strip or of interleaving any material between the side edges of the strip.
- each stack is off set by one half of the length of the sheet element.
- the fold line 25A of the sheet element 12A is off set from the fold line 25 of the sheet element 12 by a distance equal to one half of the length of the sheet element from the fold line 25A to the cut line 34.
- the nesting effect of the stack provides an integral package structure when these are brought together and wrapped by the packaging material as described hereinafter.
- an arrangement can be provided in which the position of the fold lines relative to the sheet elements is of less importance and it is possible to accept a fold line 35A at a position along the length of the sheet element different from the intended cut line 35.
- the fold lines are aligned but the sheet elements are longitudinally offset.
- the package structure can be directly rectangular apart from the outside edges which are shaped to follow the side edges of the outermost package bodies.
- the package is wrapped by a flexible packaging material preferably of heat sealable non-permeable plastics which encompasses the whole of the package as indicated at 40 (not shown in figure 1).
- the packaging material forms a sealed package which allows air to be extracted from the package and this vacuum action can be used with physical compression D from the top and bottom 13 and 14 of the package so as to compress the package to a reduced height in a vacuum packaging system.
- the amount of compression can be determined so as to minimize the volume of the package without interfering with the required loft of the product when withdrawn from the package.
- the package structure avoids the necessity for rigid sides of a box or similar container so the package structure is stable due to the compression of the layers to reduce the height of the layers and due to the pressure of each layer against the sides of the next adjacent layers.
- Compression of the package is only possible in the direction D which is at right angles to the surfaces of the portions of the strip. This acts to compress the height of the stacks so that the thickness of each strip portion in the direction D is reduced by that compression. Compression along the portions or at right angles to the stacks is not possible since this will act to distort the strip.
- Mechanical compression therefore of the package in the direction D thus reduces the dimension of the package in that direction allowing the air to be withdrawn from the flexible packaging material 40 causing the packaging material to be pulled down onto the package to maintain it in its compressed condition and to apply pressures tending to hold the stacks in intimate contact.
- the strip of each layer is connected to the next by a traverse or spliced portion of the strip which extends from one stack to the next so as to form a continuous strip through the full length of the package.
- the technique for connecting the strip of each stack to the next layer is shown in figure 7.
- the spliced portion is simply omitted for convenience of illustration.
- four stacks 200, 201, 202 and 203 are shown.
- the strip of each stack is continuous from a top strip portion 205 to a bottom strip portion 206.
- the connection is effected by a tail portion 208 which extends from the bottom portion 206 beyond one end of the stack.
- the portion 208 extends along the end of the stack at 216 and includes a twist 215 with fold lines 213 and 214 to form a portion 217 extending along the end of the next adjacent stack.
- the portion 217 is connected by a splice 211 to the top portion 205 of the next adjacent stack. Other splicing arrangements are possible.
- a web 50 is supplied on a master roll 51 and is unwound from the master roll by a feeding and guide system 52 including two nip roller pairs 53 and 54.
- a slitting system 55 is mounted transversely to the web for dividing the web into a plurality of parallel side by side strips.
- This can be provided by a slitter bar which carries a plurality of slitter knives at transversely spaced positions so as to slit the web into a plurality of strips 57 which are carried forwardly by the guide system 52 so that they are maintained in the common plane of the web and are maintained edge to edge.
- the slitting system comprises a die cutting roller 56 which rolls on a platen 56A so as to cut the strips into the wider and narrower portions described hereinbefore.
- the strips 57 are split apart by a suitable guide system well known to one skill in the art and alternate ones of the strips are passed over a diverting roller 91 which increases the path length by a distance equal to one half of the length of a sheet element so as the strips pass through the guide rollers 58 they are aligned into the position shown in figure 5.
- the strips 57 are fed over a guide roller 58 into a folding system generally indicated at 59 located underneath the feed roller 58.
- the folding system 59 comprises a support table 60 having a width sufficient to receive the full width of the web 50 when stretched out as shown in figure 5, that is the strips in side by side arrangement.
- the support table 60 has a length sufficient to receive the portions of the folded strips in the structure as previously described.
- the table 60 is mounted upon a jacking system 61 which is shown only schematically and acts to raise and lower the table so that the table is gradually lowered as the strips are folded onto the table.
- the folding system further includes a pair of folding bars 62 and 63 which act to fold the strips back and forth across the table 60.
- the folding bar 62 is mounted on an actuating cylinder 64 and similarly the folding bar 63 is mounted on an actuating cylinder 65.
- the folding bar 63 is shown in the retracted position and the folding bar 62 is shown in the extended position.
- the folding bars move alternately between these positions so that the folding bar 62 is firstly retracted and then the folding bar 63 is extended so as to move the strips across the table to form the overlying portions of the strip previously described.
- the folding bars 62 and 63 extend across the full width of the web so as to engage all of the strips simultaneously and to move those strips simultaneously into the folded positions.
- the strips thus remain in the above described position as they are being folded.
- the folding bars 62 and 63 may be in the form of rollers to allow the material to pass over the bar without friction while the material is being pushed by the bar to the required position on the table.
- the mounting system for supporting the cylinders is not shown for convenience of illustration and this will of course be well apparent to one skilled in the art.
- the folding system further includes a pair of creasing jaws 66 and 67 each arranged at the end of the stroke of a respective one of the folding bars.
- the creasing jaws also extend across the full width of the web and comprise a pair of jaw elements 68 and 69 which can be moved from an open position as indicated on the left and a closed creasing position as indicated on the right.
- the jaws are moved between these positions by an actuating cylinder 70 timed in relation to the operation of the cylinder 64 and 65.
- the creasing jaws In addition to the opening and closing movement, the creasing jaws also move inwardly and outwardly in a horizontal direction relative to the table so as to release each fold or crease line after it is formed to allow that layer and the fold at the end of the layer to be dropped onto the previous layers and to move downwardly with the table 60.
- the creasing jaw 66 at the completion of the crease moves outwardly away from the crease or fold line and at the same time opens slightly to release the fold between the two portions to drop downwardly onto the underlying portions.
- the jaws then open and move back inwardly ready to receive the portion of the strips wrapped around the folding bar and to grasp those as they are released from the folding bar as shown at the creasing jaw 67 in Figure 5.
- This compound motion can be effected by suitable mechanical linkage operated by the actuating cylinder 70, this arrangement again being well apparent to one skilled in this art.
- the strips are therefore simultaneously laid down in portions folded back and forth on top of one another to simultaneously form a plurality of the stacks of the package structure. Each stack is thus formed by a single respective one of the strips.
- the strip is continuous throughout the stack.
- one or more master rolls may be spliced into the supply with the splice being formed across the width of the web so that each slit strip also acts to slit through the splice.
- a modified method not part of the invention for manufacturing the package of the structure as shown in Figures 1 and 2 uses basically the steps shown in Figures 3, 4 and 5 but instead of using the slitter system 55 uses the cutting method shown in and described in e.g. US-A-5956 926 in which a folded web is cut using a band knife across the folded structure.
- Such an arrangement will form a package structure in which the individual package bodies are fully nested with the fold lines aligned so that is not possible to manufacture such a structure in which the fold lines are all located at the intended cut lines of the sheet elements.
- each individual strip separated from the slitting system 55 can be transported to an individual folding head where the strip is folded back and forth as previously describe to form individual package bodies.
- the individual package bodies When the individual package bodies are so formed, they can be collated and nested on a suitable collation platform for subsequent compression and wrapping as previously described.
- a marker 56B is located adjacent the folding system 59 for applying a machine readable marking 56C on the strip in registration with the intended cutting lines for dividing each sheet element from the next.
- the markings shown as a chain dot line in figures 2 and 6 can comprise an ink jet marking, possibly in the form of a dot or square, visible both to the eye and to the machine or in some cases just to the machine.
- the marking may or may not be located directly at the cut line depending upon the location of the machine reader relative to the cutting blade and in the example shown, the marking is located in advance of the intended cut line.
- the marking may extend only across a short part of the width of the strip. It will be appreciated that as the markings are registered with respective ones of the cut lines, each marking is offset from its associated cut line by the same distance.
- each intended cut line can be marked and therefore there will be a plurality of markings on each strip portion.
- FIG. 8 there is shown schematically the unfolding and cutting line for using the strip and separating the strip into the separate sheet elements.
- the package is indicated at 10 and the strip is withdrawn from the package over a guide member 80 for directing into an operating line 81.
- a cutting device 82 is operated by a control unit 83 which receives registration information from the markings 56C as read by a reader 84.
- the markings are located at a position to operate the control device to effect cutting at the intended cut line.
- the cut lines are located at the fold lines. Depending upon tolerances, the cut may not be effected directly at the fold line but may deviate slightly therefrom.
- the cut line can deviate from the fold line by a small amount provided the fold line does not end up in a central area 85 of the final product, indicated by dash lines 86, 87. That is the fold lines are arranged sufficiently close to an end of the sheet elements to avoid compromising the performance of the sheet elements.
Landscapes
- Packages (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
- Battery Mounting, Suspending (AREA)
- Making Paper Articles (AREA)
Description
- Strips of material are used for manufacture of diapers and other absorbent products. The strips are cut on the manufacturing line at longitudinally spaced transverse cut lines to divide the strip into individual sheet elements each used in the manufacture of a respective absorbent product. Generally these strips are also die cut to provide different widths for shaping of the products to better match the body of the user and for better aesthetics. Most current processes of this type die cut the elements from a single strip of the material having a width at least equal to the maximum required width and discard the waste at the sides formed by cutting away the side portions to the narrower scalloped width. Attempts are made to recycle the waste portions, generally by grinding and returning the materials to the strip manufacturer. However, recent developments have increased the complexity of the materials thus increasing the cost and making recycling more difficult. There is therefore pressure to reduce the amount of waste.
- It has been previously proposed to slit longitudinally a web of the required materials into a plurality of side by side strips which have varying width. The shaping is arranged so that the strips have the wider portion of one adjacent to the narrower portion of the next and vice-versa. This eliminates or at least reduces the amount of waste relative to an arrangement in which all sheet elements are cut individually from a respective strip of constant width.
- However the packaging of such continuous strips is problematic as the strip of elements are of varied width so that the location of the side edges varies. One proposal is to form the strip into a single roll or pad which is wound spirally. Another proposal is to wind the strip in a traverse package. Neither package structure is stable since the side edges of one wound layer do not directly overlie the side edges of the next leaving overhanging portions and feathered edges.
- Previously packages of a continuous strip of material have been formed using a technique known as "festooning" in which the strip is folded back and forth to lay a series of strip portions back and forth with each portion being folded relative to the next about a line transverse to the strip. The technique of festooning has been available for many years and is used in packaging many different types of materials but particularly material of a fibrous nature such as fabric, non-woven strips and the like. In this technique, the strip is conventionally guided into a receptacle such as a cardboard box while a first reciprocating movement causes portions of the strip to be laid across the receptacle and folded back and forth and a second reciprocating movement causes the positions of the portions to be traversed relative to the receptacle transversely to the portions. Normally the receptacle comprises a rigid rectangular container at least partly of cardboard having a base and four upstanding sides.
- Festooning can be used for packaging the strips of varying width but this technique has significant disadvantages which inhibit the effectiveness of the product when removed and processed. In particular the fold lines which are essential to the process will interfere with the absorbency or other performance of the material when such fold lines occur at a central area of the sheet element.
- US-A-5,956,926 discloses a method according to the preamble of claim 1.
- It is the object of the present invention to provide an improved method of forming a package from a ship of material.
- According to the aspect of the invention there is provided a method of forming a package of a strip of sheet material comprising the features recited in claim 1.
- Preferred features are described in the dependent claims.
- One embodiment of the invention and some Examples which are not part of the invention will now be described in conjunction with the accompanying drawings in which:
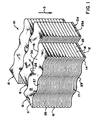
- Figure 1 is a schematic isometric view of a package of a continuous strip (not part of the present invention), the package including a plurality of layers of the strip and being shown with the flexible packaging material omitted for convenience of illustration.
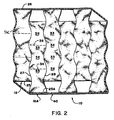
- Figure 2 is a top plan view of the package of Figure 1, with the flexible packaging material included.
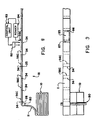
- Figure 3 is an end elevational view of an apparatus and method for forming the package of Figure 1.
- Figure 4 is a top plan view of the apparatus of Figure 5.
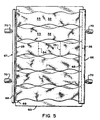
- Figure 5 is a top plan view of the platform of the apparatus of figure 4 showing the strips in spread arrangement for folding side by side.
- Figure 6 is a top plan view of a package structure formed employing the method of the invention.
- Figure 7 is an isometric view of a package of the type according to figure 6 showing the spliced connections of each strip to the next but for convenience of illustration the strips are shown of constant width.
- Figure 8 is a schematic side elevational view of a manufacturing line for cutting the strip into sheets.
- Figure 9 is a top plan view of the line of figure 8.
- In the drawings like characters of reference indicate corresponding parts in the different figures.
- As shown in Figures 1 and 2, the package comprises a generally
rectangular body 10 formed from a strip 11 of a material to be packaged and generally this material will be of a fibrous nature formed by woven or non-woven material although this is not essential to the package structure. Many materials of various thicknesses can be packaged using the festooning technique provided they can accept the creasing necessary at the end of each portion. - The package body is formed of a plurality of side by side stacks of the strip where each stack comprises a plurality of folded strip portions of the strip which are laid on top of one another. Thus as shown in Figure 1 the portions are folded back and forth at respective
end fold lines ends side edges side edges 27 of the stack and similarly, theside edges 28 of the strips of the stacks define a second set of lines in the common plane at right angles to the strip portions which contain all theside edges 28 of the stack. - Thus the package is formed by stacking the portions each on top of the next from a
bottom portion 29 up to atop portion 30 to form the stack. The package is thus formed from the plurality ofstacks 12 each of which has a length equal to that of the other stacks and therefore equal to that of the package and the stacks are formed up to a common height which is therefore equal to the height of the package. Thepackage 10 is formed from a plurality ofindividual stacks 12 arranged side by side. In figure 1 there are shown only three such stacks for convenience of illustration whereas in figure 2 there are shown six such stacks arranged side by side forming a complete package structure. Each stack is formed from a folded strip which is continuous through the stack. Each stack has atop end 13, a bottom end 14, twoends sides - It will of course be appreciated that the dimensions of the package can be varied in according to the requirements so that the number of stacks can be increased or decreased, the length and height of each stack can be varied to increase the number of folded strip portions and to increase the length of the folded strip portions.
- As best shown in figure 2 in the plan view of the strips, the strips of each stack are folded back and forth from the
fold lines 25 to thefold lines 26 to form a folded strip portion having a length equal to the distance between the fold lines. - As described hereinafter, the strips are cut so that they have a varying width between the
side edges narrow sections 32 andwider sections 33. More complex width variations can be employed in other examples. - In the example shown, the strip is intended for manufacturing diapers or similar products which are formed each from a respective sheet element cut from the length of the strip. Each sheet element in the example shown has an intended
cut line 34 at thewider section 33 and a second intendedcut line 35 also at thewider section 33 so that thenarrower section 32 is located between the intended cut lines. - It will be appreciated that in the package structure as shown, no cutting of the strips in the transverse direction has yet occurred and the
cut lines - The strip has a varying characteristic along its length which determines the position of the sheet elements on the strip and therefore determines the positions of the intended cut lines. In the example shown the varying characteristic is the varying width. Other characteristics such as additional materials or varying thickness can be used.
- It will be noted therefore from figure 2 that each folded strip portion of each of the package bodies is defined by an exact whole number of sheet elements. In the example shown the number of sheet elements is three but this can of course be varied from a minimum of one up to a maximum which depends solely upon to maximum allowable size of the transportable package structure. In most cases it is preferred that the folded strip portion will contain more than one sheet element since the sheet elements are often of the order of six inches (15.2cm) to two feet (61 cm) in length and the required package structure will be generally significantly larger than this and certainly of the order of four feet (122 cm) in length.
- In the example shown, the design of the wider and narrower portions of the strip is arranged such that no waste is formed when the slitting action occurs and the wider portions match exactly with the narrower portions of the next strips. However it is possible in some examples that there will not be an exact match between the wider portions of one strip and the narrower portions of the next adjacent strip so that some waste pieces will be formed by cutting out of the structure and discarding of those waste pieces.
- Thus as shown in figure 2, the strip portions will nest each exactly along side the next with the narrower portions of one receiving the wider portions of the next. In a situation where the wider portions do not exactly match the narrower portions, there will still be some nesting effect even though there may be spaces left between the folded strip portions.
- The fact that each folded strip portion contains an exact whole number of sheet elements ensures that the cut lines occur directly at the fold lines. Thus there are no fold lines across the strip in any part of the sheet elements after the sheet elements are cut along the cut lines. This is desirable in that the absence of fold lines in the material of the sheet elements will avoid compromising the performance or absorbency of the sheet element in the main body of the sheet element.
- Furthermore, the fact that the folded strip portion contains a whole number of the sheet elements and the sheet elements are identical ensures that the side edges of the each folded strip portion lie directly on top of the side edges of the previously laid folded strip portions. There are no overhanging or feathered edge portions therefore and all parts of the strip are fully contained within the stack. The stack is therefore in effect a solid structure having a constant density across its width. When compressed therefore the stack can form a very rigid structure with no possibility of damaging the side edges of the strip or of interleaving any material between the side edges of the strip.
- In the examples shown in figure 2, in order to provide the nesting effect, because all of the package bodies are in effect identical with the fold lines arranged across the wider part of the strip, it is necessary to off set each stack relative to the next in a direction longitudinal of the strip. This is in contrast to the gist of the invention. Thus each stack is off set by one half of the length of the sheet element. Thus for example the
fold line 25A of thesheet element 12A is off set from thefold line 25 of thesheet element 12 by a distance equal to one half of the length of the sheet element from thefold line 25A to thecut line 34. However the nesting effect of the stack provides an integral package structure when these are brought together and wrapped by the packaging material as described hereinafter. - As shown in figure 6, with the method of the invention, an arrangement can be provided in which the position of the fold lines relative to the sheet elements is of less importance and it is possible to accept a
fold line 35A at a position along the length of the sheet element different from the intendedcut line 35. Thus there is no necessity to offset the stacks longitudinally since thefold lines 35A at alternate ones of the stacks are arranged at thenarrower parts 32 of the strip. Thus the fold lines are aligned but the sheet elements are longitudinally offset. In such a manner, the package structure can be directly rectangular apart from the outside edges which are shaped to follow the side edges of the outermost package bodies. - The package is wrapped by a flexible packaging material preferably of heat sealable non-permeable plastics which encompasses the whole of the package as indicated at 40 (not shown in figure 1). The packaging material forms a sealed package which allows air to be extracted from the package and this vacuum action can be used with physical compression D from the top and bottom 13 and 14 of the package so as to compress the package to a reduced height in a vacuum packaging system. The amount of compression can be determined so as to minimize the volume of the package without interfering with the required loft of the product when withdrawn from the package. In this way the package structure avoids the necessity for rigid sides of a box or similar container so the package structure is stable due to the compression of the layers to reduce the height of the layers and due to the pressure of each layer against the sides of the next adjacent layers.
- Compression of the package is only possible in the direction D which is at right angles to the surfaces of the portions of the strip. This acts to compress the height of the stacks so that the thickness of each strip portion in the direction D is reduced by that compression. Compression along the portions or at right angles to the stacks is not possible since this will act to distort the strip. Mechanical compression therefore of the package in the direction D thus reduces the dimension of the package in that direction allowing the air to be withdrawn from the
flexible packaging material 40 causing the packaging material to be pulled down onto the package to maintain it in its compressed condition and to apply pressures tending to hold the stacks in intimate contact. - The strip of each layer is connected to the next by a traverse or spliced portion of the strip which extends from one stack to the next so as to form a continuous strip through the full length of the package. The technique for connecting the strip of each stack to the next layer is shown in figure 7. In figures 1 to 6, the spliced portion is simply omitted for convenience of illustration. Thus in figure 7 four
stacks top strip portion 205 to abottom strip portion 206. The connection is effected by atail portion 208 which extends from thebottom portion 206 beyond one end of the stack. Theportion 208 extends along the end of the stack at 216 and includes atwist 215 withfold lines portion 217 extending along the end of the next adjacent stack. Theportion 217 is connected by asplice 211 to thetop portion 205 of the next adjacent stack. Other splicing arrangements are possible. - Turning now to Figures 3, 4 and 5, a technique for forming the package structure is shown in more detail. A
web 50 is supplied on amaster roll 51 and is unwound from the master roll by a feeding andguide system 52 including two nip roller pairs 53 and 54. A slittingsystem 55 is mounted transversely to the web for dividing the web into a plurality of parallel side by side strips. This can be provided by a slitter bar which carries a plurality of slitter knives at transversely spaced positions so as to slit the web into a plurality ofstrips 57 which are carried forwardly by theguide system 52 so that they are maintained in the common plane of the web and are maintained edge to edge. However, preferably the slitting system comprises adie cutting roller 56 which rolls on aplaten 56A so as to cut the strips into the wider and narrower portions described hereinbefore. - In order to form the package structure shown in figures 1 and 2 where the fold lines are arranged at the wider parts of the strip, it is necessary to spread the strips apart to take up the position shown in figure 5 and also to longitudinally off set the strips so that the
wider portions 33 are aligned across the web and thenarrower portions 32 are also aligned across the web. This movement is effected in a zone generally indicated at 90 which occurs between therollers 54 and aguide roller 58. In thiszone 90, thestrips 57 are split apart by a suitable guide system well known to one skill in the art and alternate ones of the strips are passed over a divertingroller 91 which increases the path length by a distance equal to one half of the length of a sheet element so as the strips pass through theguide rollers 58 they are aligned into the position shown in figure 5. - The
strips 57 are fed over aguide roller 58 into a folding system generally indicated at 59 located underneath thefeed roller 58. Thefolding system 59 comprises a support table 60 having a width sufficient to receive the full width of theweb 50 when stretched out as shown in figure 5, that is the strips in side by side arrangement. The support table 60 has a length sufficient to receive the portions of the folded strips in the structure as previously described. The table 60 is mounted upon a jackingsystem 61 which is shown only schematically and acts to raise and lower the table so that the table is gradually lowered as the strips are folded onto the table. - The folding system further includes a pair of folding bars 62 and 63 which act to fold the strips back and forth across the table 60. The
folding bar 62 is mounted on anactuating cylinder 64 and similarly the folding bar 63 is mounted on anactuating cylinder 65. In Figure 3, the folding bar 63 is shown in the retracted position and thefolding bar 62 is shown in the extended position. The folding bars move alternately between these positions so that thefolding bar 62 is firstly retracted and then the folding bar 63 is extended so as to move the strips across the table to form the overlying portions of the strip previously described. The folding bars 62 and 63 extend across the full width of the web so as to engage all of the strips simultaneously and to move those strips simultaneously into the folded positions. The strips thus remain in the above described position as they are being folded. The folding bars 62 and 63 may be in the form of rollers to allow the material to pass over the bar without friction while the material is being pushed by the bar to the required position on the table. The mounting system for supporting the cylinders is not shown for convenience of illustration and this will of course be well apparent to one skilled in the art. - The folding system further includes a pair of creasing
jaws jaw elements actuating cylinder 70 timed in relation to the operation of thecylinder jaw 66 at the completion of the crease moves outwardly away from the crease or fold line and at the same time opens slightly to release the fold between the two portions to drop downwardly onto the underlying portions. The jaws then open and move back inwardly ready to receive the portion of the strips wrapped around the folding bar and to grasp those as they are released from the folding bar as shown at the creasingjaw 67 in Figure 5. This compound motion can be effected by suitable mechanical linkage operated by theactuating cylinder 70, this arrangement again being well apparent to one skilled in this art. - The strips are therefore simultaneously laid down in portions folded back and forth on top of one another to simultaneously form a plurality of the stacks of the package structure. Each stack is thus formed by a single respective one of the strips. The strip is continuous throughout the stack. In order to provide a continuous strip, one or more master rolls may be spliced into the supply with the splice being formed across the width of the web so that each slit strip also acts to slit through the splice.
- The back and forth folding of the strips into the stacks is continued until sufficient of the portions are applied to the stack to complete the stack in accordance with the required dimensions of the stack.
- A modified method not part of the invention for manufacturing the package of the structure as shown in Figures 1 and 2 uses basically the steps shown in Figures 3, 4 and 5 but instead of using the
slitter system 55 uses the cutting method shown in and described in e.g. US-A-5956 926 in which a folded web is cut using a band knife across the folded structure. Such an arrangement will form a package structure in which the individual package bodies are fully nested with the fold lines aligned so that is not possible to manufacture such a structure in which the fold lines are all located at the intended cut lines of the sheet elements. - In a yet further modified method for manufacturing the package also not part of the invention, each individual strip separated from the slitting
system 55 can be transported to an individual folding head where the strip is folded back and forth as previously describe to form individual package bodies. When the individual package bodies are so formed, they can be collated and nested on a suitable collation platform for subsequent compression and wrapping as previously described. - A
marker 56B is located adjacent thefolding system 59 for applying a machinereadable marking 56C on the strip in registration with the intended cutting lines for dividing each sheet element from the next. The markings shown as a chain dot line in figures 2 and 6 can comprise an ink jet marking, possibly in the form of a dot or square, visible both to the eye and to the machine or in some cases just to the machine. The marking may or may not be located directly at the cut line depending upon the location of the machine reader relative to the cutting blade and in the example shown, the marking is located in advance of the intended cut line. The marking may extend only across a short part of the width of the strip. It will be appreciated that as the markings are registered with respective ones of the cut lines, each marking is offset from its associated cut line by the same distance. In an arrangement in which only the fold lines are marked by the ink jet marking, there will be only one marking on each strip portion. In an arrangement in which the number of sheet elements on each strip portion is a whole number greater than one, each intended cut line can be marked and therefore there will be a plurality of markings on each strip portion. - Turning now to figures 8 and 9, there is shown schematically the unfolding and cutting line for using the strip and separating the strip into the separate sheet elements. Thus the package is indicated at 10 and the strip is withdrawn from the package over a
guide member 80 for directing into an operatingline 81. A cuttingdevice 82 is operated by acontrol unit 83 which receives registration information from themarkings 56C as read by areader 84. Thus the markings are located at a position to operate the control device to effect cutting at the intended cut line. - As explained previously, some of the cut lines are located at the fold lines. Depending upon tolerances, the cut may not be effected directly at the fold line but may deviate slightly therefrom. As the sheet elements are often intended to be stitched or otherwise formed into a final product, with edges of the sheet element thus being formed into edges of the final product, the cut line can deviate from the fold line by a small amount provided the fold line does not end up in a
central area 85 of the final product, indicated bydash lines
Claims (7)
- A method of forming a package (10) from a strip (11) of material,
comprising the step of folding the strip (11) repeatedly back and forth to form a stack (12), wherein the folded strip portions of the stack (12) are so arranged as to form a plurality of first fold lines (26) arranged at one (15) of two opposed ends of the stack (12) and a plurality of second fold lines (25) arranged at the other end (16) of the stack (12),
wherein the width of the strip (11) varies along its length,
and wherein the folded strip portions of the stack (12) are superimposed with the side edges (27, 28) thereof directly aligned such that the areas of maximum width of the folded strip portions are superimposed, and the areas of minimum width of the folded strip portions are superimposed,
characterized in that
the above step is carried out a plurality of times to form a package of a plurality of stacks (12) arranged side by side in a common package structure with alternate stacks having the first and second fold lines thereof offset from the first and second fold lines of the next adjacent stacks in a direction longitudinal to and relative to the strip portions of the stacks such that the fold lines (26) at one end (15) of all the stacks (12) are aligned so as to lie in a first common plane at one end of the package, and the fold lines (25) at the other end (16) of all the stacks (12) are aligned so as to lie in a second common plane at the other end of the package, so that the stacks (12) are not longitudinally offset with respect to one another,
wherein the stacks are nested such that areas of minimum width of each stack (12) lie alongside areas of maximum width of an adjacent stack (12). - The method according to claim 1, wherein the strip (11) in each stack (12) is continuous from an end connecting portion (205) at one end of the stack to an end connecting portion (208) at an opposed end of the stack and including splicing one end connecting portion (208) of the strip (11) from each stack (12) to an end connecting portion (205) of the strip (11) of an adjacent stack (12) by a splice connecting portion (211) of the strip (11) so as to form the strip (11) that is continuous along its length through the package.
- The method according to claim 2, including arranging the stacks substantially upright with a bottom (14) and a top (13), two sides (17,18) parallel to the edges (27,28) of the strips of the stacks, and the two ends (15,16) containing the fold lines of the stacks, and connecting the end connecting portion (208) of the bottom of one stack (12) to the end connecting portion (205) of the top of an adjacent stack (12) to form the splice connecting portion (211) which extends along one end of the stack (12).
- The method according to claim 1, including compressing the package (10) downwardly (D) so as to decrease the height of the stacks (12) from a rest height to a compressed height, and engaging the package by packaging material (40) which maintains the compression.
- The method according to claim 4, wherein the compression is sufficient to reduce the thickness of each strip portion of said stacks (12).
- The method according to anyone of the preceding claims, wherein the strip provided is fibrous.
- The method according to claim_ 4, including wrapping the package by a flexible packaging material to form a closed bag, withdrawing air, and sealing the bag against ingress of air.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/US2001/004470 WO2002064472A1 (en) | 1999-08-09 | 2001-02-12 | Packaging a strip of material for use in cutting into sheet elements arranged end to end |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1360134A1 EP1360134A1 (en) | 2003-11-12 |
| EP1360134B1 true EP1360134B1 (en) | 2007-01-17 |
Family
ID=28673369
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01909139A Expired - Lifetime EP1360134B1 (en) | 2001-02-12 | 2001-02-12 | Method of forming a package from a strip of material |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1360134B1 (en) |
| CA (1) | CA2436441C (en) |
| DE (1) | DE60126152T2 (en) |
| ES (1) | ES2280342T3 (en) |
| WO (1) | WO2002064472A1 (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102018118937A1 (en) * | 2018-08-03 | 2020-02-06 | Schmale-Holding Gmbh & Co. | Method and device for forming a loop |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5956926A (en) * | 1997-06-19 | 1999-09-28 | Kt Holdings, Inc. | Packaging a strip of material by folding and cutting the folded package |
| HUP0004788A3 (en) * | 1997-06-19 | 2002-06-28 | Bki Holding Corp Wilmington | Packaging a strip of material and a method to form it |
-
2001
- 2001-02-12 CA CA002436441A patent/CA2436441C/en not_active Expired - Fee Related
- 2001-02-12 EP EP01909139A patent/EP1360134B1/en not_active Expired - Lifetime
- 2001-02-12 DE DE60126152T patent/DE60126152T2/en not_active Expired - Lifetime
- 2001-02-12 WO PCT/US2001/004470 patent/WO2002064472A1/en not_active Ceased
- 2001-02-12 ES ES01909139T patent/ES2280342T3/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| CA2436441C (en) | 2008-07-29 |
| WO2002064472A1 (en) | 2002-08-22 |
| DE60126152T2 (en) | 2007-10-18 |
| CA2436441A1 (en) | 2002-08-22 |
| EP1360134A1 (en) | 2003-11-12 |
| DE60126152D1 (en) | 2007-03-08 |
| ES2280342T3 (en) | 2007-09-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6336307B1 (en) | Method of packaging a strip of material for use in cutting into sheet elements arranged end to end | |
| US6612097B2 (en) | Packaging a strip of material | |
| US5956926A (en) | Packaging a strip of material by folding and cutting the folded package | |
| EP3471954B1 (en) | Box forming machine | |
| US4475730A (en) | Apparatus for folding and stacking paper products | |
| US5927051A (en) | Packaging a continuous strip of material | |
| US6729471B2 (en) | Packaging a strip of material with compression to reduce volume | |
| US20030070396A1 (en) | Packaging a strip of material in side by side stacks spliced end to end | |
| US6321511B1 (en) | Packaging a strip of material with compression to reduce volume | |
| EP0910542A1 (en) | Packaging a strip of material | |
| US6293075B1 (en) | Packaging a strip of material | |
| US20040048727A1 (en) | Apparatus and method for folding and stacking napkins | |
| KR0172114B1 (en) | Machine and method for packaging folded swabs | |
| CA2436221C (en) | Packaging a strip of material of varying width | |
| US6067775A (en) | Packaging a strip of material by folding | |
| US6176068B1 (en) | Packaging a strip of material in layers with intervening splices | |
| CA2436441C (en) | Packaging a strip of material for use in cutting into sheet elements arranged end to end | |
| US6009689A (en) | Packaging a strip of material in layers | |
| WO1999016693A1 (en) | Apparatus for packaging a strip of material | |
| RU238655U1 (en) | Notebook with an integrated polymer cover | |
| US20250178764A1 (en) | Product packaging machine and method | |
| RU2751229C2 (en) | Method for compression of tissue paper | |
| GB2284178A (en) | Manufacturing paperboard blanks | |
| IES59845B2 (en) | Manufacturing paperboard blanks | |
| IE74692B1 (en) | Manufacturing paperboard blanks |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20030812 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| 17Q | First examination report despatched |
Effective date: 20040226 |
|
| RTI1 | Title (correction) |
Free format text: METHOD OF FORMING A PACKAGE FROM A STRIP OF MATERIAL |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: BKI HOLDING CORPORATION |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60126152 Country of ref document: DE Date of ref document: 20070308 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070417 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070618 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2280342 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20071018 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070418 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070117 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20090206 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110916 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080229 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20140113 Year of fee payment: 14 Ref country code: IT Payment date: 20140211 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20140212 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20140417 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 60126152 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20150212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150901 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150212 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20160329 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150213 |