EP1260618B1 - Non-woven material - Google Patents
Non-woven material Download PDFInfo
- Publication number
- EP1260618B1 EP1260618B1 EP01112487A EP01112487A EP1260618B1 EP 1260618 B1 EP1260618 B1 EP 1260618B1 EP 01112487 A EP01112487 A EP 01112487A EP 01112487 A EP01112487 A EP 01112487A EP 1260618 B1 EP1260618 B1 EP 1260618B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- lactone
- fibres
- woven
- propylene polymer
- bonding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F1/00—General methods for the manufacture of artificial filaments or the like
- D01F1/02—Addition of substances to the spinning solution or to the melt
- D01F1/10—Other agents for modifying properties
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F6/00—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof
- D01F6/02—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof from homopolymers obtained by reactions only involving carbon-to-carbon unsaturated bonds
- D01F6/04—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof from homopolymers obtained by reactions only involving carbon-to-carbon unsaturated bonds from polyolefins
- D01F6/06—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof from homopolymers obtained by reactions only involving carbon-to-carbon unsaturated bonds from polyolefins from polypropylene
Definitions
- the present invention relates to a non-woven formed by propylene polymer fibres with improved bonding properties, and a process for the production of a non-woven by bonding of webs formed by such fibres.
- a propylene polymer composition comprising further components, as e.g. an anti-oxidant or an acid scavengers, is melt extruded at temperatures of above 200 °C and fibres are spun by passing the melt through a spinnerette and quenching the produced fibres.
- Such spinning processes today are carried out at high speed in the order of 1000 m/min up to 4000 m/min but still an increase in line speed and output is desirable.
- the fibres undergo one or more stretching steps after quenching.
- non-wovens are produced by forming a web followed by a final bonding step.
- the fibres of the web are bound together, e.g. by passing the web through a calender in which heat and pressure is applied.
- the bonding process affecting the fibre surface happens within a very short time and temperature window.
- Such webs and hence non-wovens may be produced either by staple fibres, i.e. fibres which have been stapled after their production, or filaments as e.g. continuous filaments.
- staple fibres i.e. fibres which have been stapled after their production
- filaments as e.g. continuous filaments.
- the term "fibres" as used herein is intended to cover both staple fibres and filaments.
- the web forming usually comprises a carding step and the fibres are crimped before web forming.
- the filaments can be spun directly onto a moving belt before the bonding is performed e.g. with a calender (spunbonded fibres).
- thermo bonding step is one factor, which is limiting the maximum line speed and therefore an improvement of the bonding properties of the fibres in this step is desirable, which in turn effects advantageously to the web strength.
- the object of the present invention to improve the mechanical properties of a non-woven by improving the bonding properties of propylene polymer fibres.
- the present invention is targeted to improve the bonding properties of staple fibres.
- the spinning process as well as the bonding step have to be performed within a narrow temperature window. This puts severe restrictions on the process for the production of non-wovens as for obtaining high quality non-wovens the processes have to be carried out and maintained within said narrow temperature windows.
- GB 2 315 070 A discloses a stabilizer mixture for organic materials and such organic materials which possess outstanding stability to oxidative, thermal or light-induced degradation.
- the stabilizer mixture comprises at least one compound of the benzofuran-2-one type ant at least one compound of the sterically hindered amine type.
- An organic phosphite or phosphonite may also be included in the stabilizer mixture.
- the organic material may be a polymer, e.g. a polyolefin, for instance a phenol-free polyolefin fibre.
- EP 0 875 530 A1 discloses a olefin polymer composition having low smoke generation and fiber and film prepared therefrom.
- the polymer composition comprises i) an olefin polymer containing an acid neutralizing agent other than metallic salt of a saturated or unsaturated fatty acid, and ii) a stabilizer system distributed throughout the polymer, the stabilizer system comprising a) a phosphite selected from the group consisting of 2,2',2"-nitrilo[triethyl-tris(3,3',5,5'-tetra-tert.-butyl-1,1-biphenyl-2,2'-diyl)phosphite] and tris(2,4-di-tert.-butylphenyl) phosphite; and b) a N,N-dialkylhydroxylamine, a benzofuranone or mixtures thereof.
- the present invention is based on the finding that the above given object can be solved by fibres which have been produced by adding only small amounts of additives according to claim 1 to the propylene polymer composition prior to the spinning of the fibres.
- Lactones are defined as organic compounds comprising a cyclic ester group. By the term lactone also mixtures of different lactones are understood. This also applies for preferred embodiments given below.
- lactones have been in use as components of anti-oxidant compositions their ability to improve the bonding properties of polypropylene staple fibres has not yet been recognized.
- Commercial suppliers recommend the use of such anti-oxidant compositions in an amount of at least 1300 ppm wherein the amount of lactone is at least 300 ppm.
- the present invention therefore provides a non-woven formed by propylene polymer fibres with improved bonding properties, characterized in that the fibres comprise a lactone of the furan-2-one type in an amount of at most 200 ppm.
- the present invention provides a process for producing such non-wovens.
- the present invention relates to a non-woven comprising staple fibres and a process for producing such a non-woven.
- the polypropylene fibres have improved bonding properties so that they allow for the production of non-wovens with improved mechanical properties, in particular mechanical strength.
- the BI max of the inventive fibres is 20.0 or more, more preferably more than 22, most preferably 22.5 or more.
- the bonding of the web may be performed by any bonding technique known in the art as e.g. thermobonding, infrared bonding or ultrasound bonding. It is preferred that bonding is performed by thermobonding, e.g. calender bonding or hot air bonding, and further preferred bonding is performed by calender bonding.
- the bonding process is preferably performed at a speed of at least 150 m/min, more preferably at least 200 m/min and still more preferably of at least 250 m/min.
- inventive fibres allow for a broad spinning window, i.e. a broad temperature range within which the spinning process for the production of the fibres can be performed, as well as a broad bonding window by calender bonding, i.e. the temperature range within which the bonding step can be carried out, with the fibres still showing improved bonding index.
- a broad spinning window i.e. a broad temperature range within which the spinning process for the production of the fibres can be performed
- calender bonding i.e. the temperature range within which the bonding step can be carried out
- the bonding window is defined the temperature interval in which a bonding index in the non-woven is obtained which differs from the maximum bonding index BI max obtained at optimum bonding temperature by not more than 15 %. In case of a typical good quality non-woven for use e.g. in hygienic absorbent products this corresponds to a difference in the bonding index of about 3 N/5cm compared to BI max .
- a broad bonding window gives the producer of non-woven fabrics a better possibility of obtaining a uniform product even when using a calendering system with temperature variation over the calender surface or when using a higher bonding speed or lower bonding temperature. This is a considerable advantage for the non-woven producer.
- the spinning window is defined as the temperature interval in which a bonding index in the non-woven is obtained which differs from the maximum bonding index BI max obtained at optimum spinning temperature by not more than 15 %.
- furan-2-one type designates all chemical compounds comprising a furan-2-one group
- the inventive non-woven comprises a lactone of the furan-2-one type in an amount of 170 ppm or less, still more preferred of 140 ppm or less and most preferred of 120 ppm or less.
- the lactone is of the benzofuran-2-one type.
- benzofuran-2-one and all kinds of possible derivatives made by any kind of substitution are meant.
- Such compounds are represented by formula (I), wherein R 1 is any kind of substituent other than H, preferably substituted or non-substituted phenyl, and R 2 to R 6 independently are H or any kind of other substituent, preferably alkyl.
- the above-mentioned lactone is of the benzofuran-3-phenyl-2-one type.
- This term designates benzofuran-3-phenyl-2-one and all possible derivatives thereof made by any kind of substitution.
- These compounds are represented by formula (I) wherein R 1 is a phenyl group which may also be substituted by any kind of substituent, preferably alkyl.
- the lactone comprises benzofuran-3-phenyl-2-one, an alkyl substituted derivative thereof, or a mixture of any of such compounds.
- R 1 is phenyl group which may further be substituted with alkyl substituents, preferably C 1 - C 4 alkyl, and R 2 to R 5 independently is H or alkyl, preferably H or C 1 - C 6 alkyl.
- the lactone comprises 5,7-di-tert-butyl-3-phenyl-2-one, a methyl substituted derivative thereof or a mixture of any of such compounds.
- These compounds are represented by formula (I) wherein R 2 and R 4 are tert-butyl, R 3 and R 5 are H, R 1 is phenyl which may further be substituted with one or more methyl groups.
- the lactone comprises a compound selected from the group of 5,7-di-tert-butyl-benzofuran-3-phenyl-2-one, 5,7-di-tert-butyl-benzofuran-3-(3,4-dimethyl-phenyl)-2-one and 5,7-di-tert-butyl-benzofuran-3-(2,3-di-methyl-phenyl)-2-one or a mixture of any of such compounds.
- the lactone comprises Irganox HP-136 of Ciba Speciality Chemicals, which is a mixture of the two last mentioned compounds.
- the inventive non-woven comprises the lactone in an amount of 50 ppm or more, more preferred of 70 ppm or more, still more preferred of 90 ppm or more and most preferred of 100 ppm or more.
- the non-woven further comprises an organic phosphite.
- organic phosphite Such preferred compounds are represented by formula (II): wherein X is O and R 1 to R 3 are organic residues.
- Preferred examples of the phosphite include tris(2,4-di-tert-butylphenyl)-phosphite (Irgafos 168 of Ciba Speciality Chemicals), bis-(2,4-dicumylphenyl)-pentaerythritol-diphosphite (Doverphos S-9228 of Dover), bis-(2,4-di-tert.-butylphenyl)-pentaerythrityl-di-phosphite (Ultanox 626), bis-(2-methyl-4,6-bis-(1,1-dimethylethyl)-phenyl)-phosphorous acid ethylester (Irgafos 38), phosphorous acid cyclic-butylethyl-propandiol, 2,4,6-tritert.-butylphenyl ester (Ultranox 641), bis-(2,6-di-tert.-but
- the phosphite is tris(2,4-di-tert-butyl-phenyl)-phosphite (Irgafos 168 of Ciba Speciality Chemicals), bis-(2,4-dicumylphenyl)-pentaerythritol-diphosphite (Doverphos S-9228).
- the phosphite is present in the inventive propylene polymer fibre in an amount of at least 100 parts by weight (pbw) up to at most 500 pbw with respect to 100 pbw of the lactone, more preferred in an amount of about 200 pbw with respect to 100 pbw of the lactone.
- the non-woven further comprises an UV stabilizer.
- UV stabilizers are known to the skilled person. UV stabilizers effect advantageously to the bonding index.
- UV stabilizer Tinuvin 622 of Ciba Speciality Chemicals is used.
- the UV stabilizer is present in an amount of at least 50 pbw up to at most 200 pbw with respect to 100 pbw of the lactone and more preferred in an amount of about 100 pbw with respect to 100 pbw of the lactone.
- inventive proylene polymer fibre is essentially free of compounds containing phenol groups.
- the amount of lactone, phosphite and UV stabilizer together is at most 700 ppm, more preferably at most 500 ppm in the inventive non-woven.
- the spinning temperature of the fibre is from 220 to 300 °C.
- the lower temperatures are preferably used for spunbonded fibres and higher temperatures for staple fibres.
- the spinning temperature of staple fibres is 245 °C to 270 °C.
- the calender temperature is preferably 140 °C to 155 °C.
- the invention provides a process for the production of a non-woven which is characterized in that the non-woven is produced by thermo bonding of the fibres as described above or of fibres prepared according to the process described above.
- the propylene polymer fibres preferably are produced in a high speed spinning line.
- this process further comprises a carding step in the web formation.
- non-woven from staple fibres carding is carried out at high speed, preferably at a speed of 50 m/min or higher.
- the bonding index of the non-woven is essentially determined by the bonding properties of the fibre so that improved bonding properties of the fibre give an improved bonding index of the non-woven.
- Polypropylene powder with melt flow rate MFR 2 of 12 g/10min (ISO 1133, 2,16 kg, 230 °C) was mixed with additives, extruded and pelletised with conventional extruder. Calcium stearate was used as anti-acidic agent.
- composition 1 460 ppm Fiberstab L112
- Composition 2 650 ppm Fiberstab L112
- Composition 3 (comparative): 800 ppm Irgafos 1 68 + 150 ppm Irganox 3114
- Fiberstab L112 is composed of 25 wt.% Irganox HP 136 (lactone compound), 50 wt.% Irgafos 168 (phosphite compound) and 25 wt.% Tinuvin 622 (UV stabilizer).
- the fibres had a fineness of 2.2 dTex.
- the fibres were texturised to a level of about 12 crimps/cm and cut to 40 mm staple fibres.
- Nonwoven fabrics were produced using a Hergeth monolayer/Kusters calender having a width of 600 mm.
- the winder speed of the process line was 100 m/min.
- the produced web was a web having a weight of 20 gram per square meter.
- the calander window was between 140 and 152 °C and for each fibre sample, 5 different calender temperature have been used: 140, 143, 146, 149 and 152 °C.
- thermo bonding window This also applies for the thermo bonding window. It can be seen from Fig 1 and 2 that the inventive compositions have extremely broad thermo bonding window towards the spinning temperature.
- the spinning temperature can change from 255 °C to 265 °C at constant calender temperature without any effect on the bonding index. If the calender temperature of 146 °C is selected the bonding index is close to 24 over the whole range of spinning temperatures. It is obvious that a system like this is extremely easy to handle for a fibre producer and will lead to a very consistent fibre and non-woven.
- compositions 1 and 2 accoring to the invention with an amount of 115 ppm and 160 ppm of lactone show an improved bonding index.
- Table 2 Mechanical properties of non-woven of fibres comprising composition 2 SPINNINGTEMP [°C] 260°C - MF 37 265°C - MF 44 270°C - MF 46 CODE 23 E 2 16 E 3 16 E 4 16 E 5 16 E 6 17 E 2 17 E 3 17 E 4 17 E 5 17 E 6 18 E 2 18 E 3 18 E 4 18 E 5 18 E6 CALENDER TEMP.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Textile Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Artificial Filaments (AREA)
- Nonwoven Fabrics (AREA)
- Woven Fabrics (AREA)
- Multicomponent Fibers (AREA)
- Polyesters Or Polycarbonates (AREA)
Abstract
Description
- The present invention relates to a non-woven formed by propylene polymer fibres with improved bonding properties, and a process for the production of a non-woven by bonding of webs formed by such fibres.
- In the production of non-wovens from polypropylene fibres usually in a first step a propylene polymer composition comprising further components, as e.g. an anti-oxidant or an acid scavengers, is melt extruded at temperatures of above 200 °C and fibres are spun by passing the melt through a spinnerette and quenching the produced fibres. Such spinning processes today are carried out at high speed in the order of 1000 m/min up to 4000 m/min but still an increase in line speed and output is desirable. Optionally, the fibres undergo one or more stretching steps after quenching.
- From the so produced fibres non-wovens are produced by forming a web followed by a final bonding step. In this step, the fibres of the web are bound together, e.g. by passing the web through a calender in which heat and pressure is applied. The bonding process affecting the fibre surface happens within a very short time and temperature window.
- Such webs and hence non-wovens may be produced either by staple fibres, i.e. fibres which have been stapled after their production, or filaments as e.g. continuous filaments. The term "fibres" as used herein is intended to cover both staple fibres and filaments.
- If staple fibres are used the web forming usually comprises a carding step and the fibres are crimped before web forming. On the other hand, if continuous filaments are used then the filaments can be spun directly onto a moving belt before the bonding is performed e.g. with a calender (spunbonded fibres).
- In the production of thermo bonded non-wovens the thermo bonding step is one factor, which is limiting the maximum line speed and therefore an improvement of the bonding properties of the fibres in this step is desirable, which in turn effects advantageously to the web strength.
- It is well known that additives to the propylene polymer play an important role for defining the bonding properties of the fibre and thus the mechanical properties of the non-woven. Better bonding properties of the fibres lead to improved mechanical properties, in particular mechanical strength essentially defined by the bonding index, of the non-woven.
- It is therefore the object of the present invention to improve the mechanical properties of a non-woven by improving the bonding properties of propylene polymer fibres. Especially, the present invention is targeted to improve the bonding properties of staple fibres.
- Further, for obtaining good bonding properties of the fibres usually the spinning process as well as the bonding step have to be performed within a narrow temperature window. This puts severe restrictions on the process for the production of non-wovens as for obtaining high quality non-wovens the processes have to be carried out and maintained within said narrow temperature windows.
- It is therefore a further object of the present invention to widen the temperature windows for both spinning process and bonding step without deteriously affecting the quality of the non-woven.
- US 5,281,378 decribes an improvement in thermo bonding properties of such fibres due to a combination of an optimized molecular weight distribution of the polymer and delayed queching during fibre spinning.
- GB 2 315 070 A discloses a stabilizer mixture for organic materials and such organic materials which possess outstanding stability to oxidative, thermal or light-induced degradation. The stabilizer mixture comprises at least one compound of the benzofuran-2-one type ant at least one compound of the sterically hindered amine type. An organic phosphite or phosphonite may also be included in the stabilizer mixture. The organic material may be a polymer, e.g. a polyolefin, for instance a phenol-free polyolefin fibre.
-
EP 0 875 530 A1 discloses a olefin polymer composition having low smoke generation and fiber and film prepared therefrom. The polymer composition comprises i) an olefin polymer containing an acid neutralizing agent other than metallic salt of a saturated or unsaturated fatty acid, and ii) a stabilizer system distributed throughout the polymer, the stabilizer system comprising a) a phosphite selected from the group consisting of 2,2',2"-nitrilo[triethyl-tris(3,3',5,5'-tetra-tert.-butyl-1,1-biphenyl-2,2'-diyl)phosphite] and tris(2,4-di-tert.-butylphenyl) phosphite; and b) a N,N-dialkylhydroxylamine, a benzofuranone or mixtures thereof. - The present invention is based on the finding that the above given object can be solved by fibres which have been produced by adding only small amounts of additives according to claim 1 to the propylene polymer composition prior to the spinning of the fibres. Lactones are defined as organic compounds comprising a cyclic ester group. By the term lactone also mixtures of different lactones are understood. This also applies for preferred embodiments given below.
- Although lactones have been in use as components of anti-oxidant compositions their ability to improve the bonding properties of polypropylene staple fibres has not yet been recognized. Commercial suppliers recommend the use of such anti-oxidant compositions in an amount of at least 1300 ppm wherein the amount of lactone is at least 300 ppm.
- The present invention therefore provides a non-woven formed by propylene polymer fibres with improved bonding properties, characterized in that the fibres comprise a lactone of the furan-2-one type in an amount of at most 200 ppm.
- Furthermore, the present invention provides a process for producing such non-wovens.
- In a preferred embodiment the present invention relates to a non-woven comprising staple fibres and a process for producing such a non-woven.
- The polypropylene fibres have improved bonding properties so that they allow for the production of non-wovens with improved mechanical properties, in particular mechanical strength. The improvement of the bonding properties of the fibres are measured via the measurement of the bonding index (BI) of the produced non-woven which is defined as

wherein CD is the strength of the non-woven cross-direction of the web and MD is the strength in the machine direction quoted as N/5 cm. As the strength in the MD often is different from the strength in the CD, the bonding index is a function of both of these. It is preferred that the ratio between the MD-strength and the CD-strength is around unity. - Preferably, the BImax of the inventive fibres is 20.0 or more, more preferably more than 22, most preferably 22.5 or more. The bonding of the web may be performed by any bonding technique known in the art as e.g. thermobonding, infrared bonding or ultrasound bonding. It is preferred that bonding is performed by thermobonding, e.g. calender bonding or hot air bonding, and further preferred bonding is performed by calender bonding.
- The bonding process is preferably performed at a speed of at least 150 m/min, more preferably at least 200 m/min and still more preferably of at least 250 m/min.
- Furthermore, the inventive fibres allow for a broad spinning window, i.e. a broad temperature range within which the spinning process for the production of the fibres can be performed, as well as a broad bonding window by calender bonding, i.e. the temperature range within which the bonding step can be carried out, with the fibres still showing improved bonding index. This means that the improved bonding properties of the fibres and hence the improved mechanical properties of the non-woven can be reached within broad temperature ranges both for the spinning of the fibres and the bonding step.
- The bonding window is defined the temperature interval in which a bonding index in the non-woven is obtained which differs from the maximum bonding index BImax obtained at optimum bonding temperature by not more than 15 %. In case of a typical good quality non-woven for use e.g. in hygienic absorbent products this corresponds to a difference in the bonding index of about 3 N/5cm compared to BImax.
- A broad bonding window gives the producer of non-woven fabrics a better possibility of obtaining a uniform product even when using a calendering system with temperature variation over the calender surface or when using a higher bonding speed or lower bonding temperature. This is a considerable advantage for the non-woven producer.
- The spinning window is defined as the temperature interval in which a bonding index in the non-woven is obtained which differs from the maximum bonding index BImax obtained at optimum spinning temperature by not more than 15 %.
- The term furan-2-one type designates all chemical compounds comprising a furan-2-one group
- Preferably, the inventive non-woven comprises a lactone of the furan-2-one type in an amount of 170 ppm or less, still more preferred of 140 ppm or less and most preferred of 120 ppm or less.
- Further preferred, the lactone is of the benzofuran-2-one type. By this term benzofuran-2-one and all kinds of possible derivatives made by any kind of substitution are meant. Such compounds are represented by formula (I),

R2 to R6 independently are H or any kind of other substituent, preferably alkyl. - These compounds have already been applied in stabilizing compositions or polyolefins as e.g. described in GB 2322374. Compounds of the benzofuran-2-one type further are for example described in the following documents: US 4,325,863, US 4,388,244, US 5,175,312, US 5,252,643, US 5,216,052, US 5,369,159, US 5,488,117, US 5,356,966, US 5,367,008, US 5,428, 162, US 5,428,177 or US 5,516,920. The contents of these documents is included herein by reference.
- Further preferred, the above-mentioned lactone is of the benzofuran-3-phenyl-2-one type. This term designates benzofuran-3-phenyl-2-one and all possible derivatives thereof made by any kind of substitution. These compounds are represented by formula (I) wherein R1 is a phenyl group which may also be substituted by any kind of substituent, preferably alkyl.
- Preferably, the lactone comprises benzofuran-3-phenyl-2-one, an alkyl substituted derivative thereof, or a mixture of any of such compounds. Theses compounds are represented by the above given formula (I) wherein R1 is phenyl group which may further be substituted with alkyl substituents, preferably C1 - C4 alkyl, and R2 to R5 independently is H or alkyl, preferably H or C1 - C6 alkyl.
- Further preferred, the lactone comprises 5,7-di-tert-butyl-3-phenyl-2-one, a methyl substituted derivative thereof or a mixture of any of such compounds. These compounds are represented by formula (I) wherein R2 and R4 are tert-butyl, R3 and R5 are H, R1 is phenyl which may further be substituted with one or more methyl groups.
- In a particular preferred embodiment the lactone comprises a compound selected from the group of 5,7-di-tert-butyl-benzofuran-3-phenyl-2-one, 5,7-di-tert-butyl-benzofuran-3-(3,4-dimethyl-phenyl)-2-one and 5,7-di-tert-butyl-benzofuran-3-(2,3-di-methyl-phenyl)-2-one or a mixture of any of such compounds.
- Most preferred, the lactone comprises Irganox HP-136 of Ciba Speciality Chemicals, which is a mixture of the two last mentioned compounds.
- In a preferred embodiment the inventive non-woven comprises the lactone in an amount of 50 ppm or more, more preferred of 70 ppm or more, still more preferred of 90 ppm or more and most preferred of 100 ppm or more.
- According to the invention the non-woven further comprises an organic phosphite. Such preferred compounds are represented by formula (II):
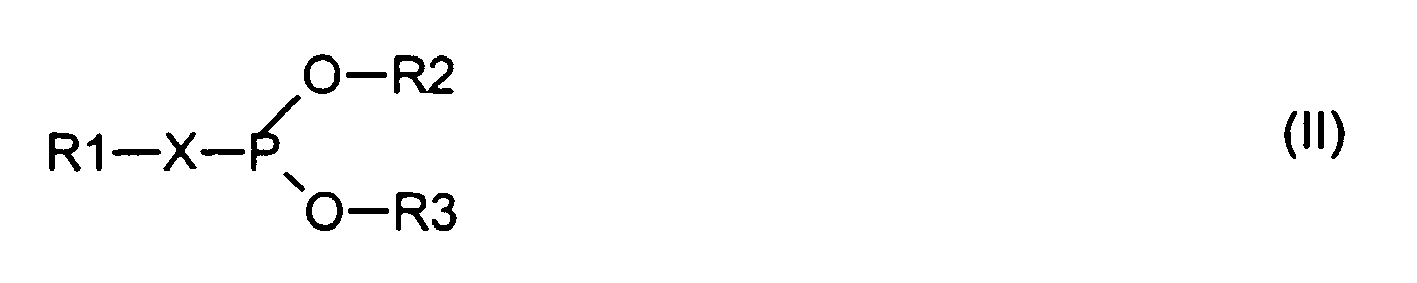
R1 to R3 are organic residues. - Such compounds are also described in GB 2322374. The contents of this document concerning phosphites is herewith enclosed by reference.
- Preferred examples of the phosphite include tris(2,4-di-tert-butylphenyl)-phosphite (Irgafos 168 of Ciba Speciality Chemicals), bis-(2,4-dicumylphenyl)-pentaerythritol-diphosphite (Doverphos S-9228 of Dover), bis-(2,4-di-tert.-butylphenyl)-pentaerythrityl-di-phosphite (Ultanox 626), bis-(2-methyl-4,6-bis-(1,1-dimethylethyl)-phenyl)-phosphorous acid ethylester (Irgafos 38), phosphorous acid cyclic-butylethyl-propandiol, 2,4,6-tritert.-butylphenyl ester (Ultranox 641), bis-(2,6-di-tert.-butyl-4-methylphenyl)-pentaerythrityl-di-phosphite (ADK STAB PEP-36) and 2,2'-methylenebis-(4,6-di-tert.-butylphenyl)-octyl-phosphite (ADK STAB HP-10).
- More preferably, the phosphite is tris(2,4-di-tert-butyl-phenyl)-phosphite (Irgafos 168 of Ciba Speciality Chemicals), bis-(2,4-dicumylphenyl)-pentaerythritol-diphosphite (Doverphos S-9228).
- Further preferred, the phosphite is present in the inventive propylene polymer fibre in an amount of at least 100 parts by weight (pbw) up to at most 500 pbw with respect to 100 pbw of the lactone, more preferred in an amount of about 200 pbw with respect to 100 pbw of the lactone.
- According to the invention the non-woven further comprises an UV stabilizer. Such UV stabilizers are known to the skilled person. UV stabilizers effect advantageously to the bonding index.
- Preferably, as UV stabilizer Tinuvin 622 of Ciba Speciality Chemicals is used.
- Further preferred, the UV stabilizer is present in an amount of at least 50 pbw up to at most 200 pbw with respect to 100 pbw of the lactone and more preferred in an amount of about 100 pbw with respect to 100 pbw of the lactone.
- In a further preferred embodiment the inventive proylene polymer fibre is essentially free of compounds containing phenol groups.
- According to the invention the amount of lactone, phosphite and UV stabilizer together is at most 700 ppm, more preferably at most 500 ppm in the inventive non-woven.
- All embodiments cited as preferred for the inventive propylene polymer fibre are also preferred for the inventive process.
- Furthermore, in a preferred embodiment of the inventive process the spinning temperature of the fibre is from 220 to 300 °C. The lower temperatures are preferably used for spunbonded fibres and higher temperatures for staple fibres. Preferably, the spinning temperature of staple fibres is 245 °C to 270 °C. The calender temperature is preferably 140 °C to 155 °C.
- The invention provides a process for the production of a non-woven which is characterized in that the non-woven is produced by thermo bonding of the fibres as described above or of fibres prepared according to the process described above.
- The propylene polymer fibres preferably are produced in a high speed spinning line.
- Preferably, when staple fibres are used this process further comprises a carding step in the web formation.
- Further preferred, in the production of the non-woven from staple fibres carding is carried out at high speed, preferably at a speed of 50 m/min or higher.
- The bonding index of the non-woven is essentially determined by the bonding properties of the fibre so that improved bonding properties of the fibre give an improved bonding index of the non-woven.
- The present invention will be further illustrated by the following examples including Figures 1 to 3 wherein
- Figure 1 shows the spinning and bonding window of proylene polymer staple fibres comprising 115 ppm of Irganox HP-136 (composition 1 of the examples).
- Figure 2 shows the spinning and bonding window of propylene polymer staple fibres comprising Irganox HP-136 in an amount of 160 ppm (composition 2 of the examples).
- Figure 3 shows the spinning and bonding window of a propylene polymer staple fibre comprising a conventional anti-oxidant system without lactone (composition 3 of the examples).
- Polypropylene powder with melt flow rate MFR2 of 12 g/10min (ISO 1133, 2,16 kg, 230 °C) was mixed with additives, extruded and pelletised with conventional extruder. Calcium stearate was used as anti-acidic agent.
- The following compositions were used in the polymers:
Composition 1: 460 ppm Fiberstab L112 Composition 2: 650 ppm Fiberstab L112 Composition 3 (comparative): 800 ppm Irgafos 1 68 + 150 ppm Irganox 3114 - Fiberstab L112 is composed of 25 wt.% Irganox HP 136 (lactone compound), 50 wt.% Irgafos 168 (phosphite compound) and 25 wt.% Tinuvin 622 (UV stabilizer).
- In the comparative composition which is commonly used as an anti-oxidant additive, no lactone component is present.
- An ESL-pilot conventional spinning line was used to produce staple fibres. The spinning temperatures were in the range of 249 to 265 °C. During spinning, the MFR2 of the polypropylene fibres increased up to approx. 40 g/10min due to thermal degradation.
- The fibres had a fineness of 2.2 dTex. The fibres were texturised to a level of about 12 crimps/cm and cut to 40 mm staple fibres.
- Nonwoven fabrics were produced using a Hergeth monolayer/Kusters calender having a width of 600 mm. The winder speed of the process line was 100 m/min. The produced web was a web having a weight of 20 gram per square meter.
- The calander window was between 140 and 152 °C and for each fibre sample, 5 different calender temperature have been used: 140, 143, 146, 149 and 152 °C.
- The mechanical properties of the produced non-wovens both in MD and CD are listed in Tables 1, 2 and 3.
- The bonding properties as a function of spinning and calander temperature are listed in Table 4 and shown in Fig. 1, 2 and 3.
- The maximum bonding indices obtained are shown in Fig. 4.
- The results as listed in Tables 1 to 3 and shown in Fig. 1 to 4 show that one of the benefits of the invention is that the spinning temperature can vary a lot and still good bonding indices are obtained, i.e. the spinning temperature and the careful control of this temperature is not that crucial as in conventional systems.
- This also applies for the thermo bonding window. It can be seen from Fig 1 and 2 that the inventive compositions have extremely broad thermo bonding window towards the spinning temperature. The spinning temperature can change from 255 °C to 265 °C at constant calender temperature without any effect on the bonding index. If the calender temperature of 146 °C is selected the bonding index is close to 24 over the whole range of spinning temperatures. It is obvious that a system like this is extremely easy to handle for a fibre producer and will lead to a very consistent fibre and non-woven.
- In contrast, in the comparative composition shown in Fig. 3 the bonding window bonding indexes higher than 20 can only be reached for a narrow range of spinning temperatures and calender temperatures.
- Further, it can be seen from Fig. 1 that compositions 1 and 2 accoring to the invention with an amount of 115 ppm and 160 ppm of lactone show an improved bonding index.

Table 2: Mechanical properties of non-woven of fibres comprising composition 2 SPINNINGTEMP [°C] 260°C - MF 37 265°C - MF 44 270°C - MF 46 CODE 23 E 2 16 E 3 16 E 4 16 E 516 E 6 17 E 2 17 E 3 17 E 4 17 E 517 E 6 18 E 2 18 E 3 18 E 4 18 E 518 E6 CALENDER TEMP. [°C ] 140 143 146 149 152 140 143 146 149 17 E 18 E 2 18 E 3 18 E 4 18 E 518 E 6 BASIC WEIGHT [g /m2] 18,5 18,4 17,7 20,9 21,4 19,3 17,5 16,9 21,8 152 140 143 146 149 152 MACHINE DIRECTION MAX. FORCE [N ] 40,5 43,2 47,7 60,6 49,6 44,3 35,1 42,2 45,3 39,6 30,1 27,9 37,9 31,0 37,1 TENACITY calc/20g/m2 [N / 5cm ] 43,8 47,0 53,9 48,4 46,4 45,9 40,1 50,0 41,6 38,0 29,2 33,0 33,5 27,0 31,7 std 4,0 3,8 3,8 4,6 4,5 3,2 4,5 5,5 6,5 3,7 5,3 6,1 5,2 4,0 2, ELONGATION [%] 37,3 44,8 53,4 52,4 44,7 49,6 34,1 48,3 41,9 31,2 19,6 22,2 22,2 15,7 19,6 std 5,8 8,8 6,7 12,9 5,6 10,6 8,2 10,1 12,1 4,9 5,6 5,2 5,8 3,2 3,6 BASIC WEIGHT [g/m2] 18,5 18,4 17,7 20,9 21,4 19,3 17,5 16,9 21,8 20,8 20,6 16,9 22,6 23,0 23,4 CROSS DIRECTION MAX. FORCE [N] 4,4 5,9 8,3 9,8 11,0 7,3 7,2 8,1 9,4 10,2 3,7 3,5 5,8 6,9 7,3 TENACITY calc/20g/m2 [N / 5 cm ] 4,8 6,4 9,4 9,3 10,3 7,6 8,3 9,6 8,6 9,8 3,6 4,1 5,1 6,0 6,2 std 1,2 0,9 0,7 0,5 0,9 1,5 1,8 1,6 1,6 0,8 1,2 1,4 1,2 1,6 1,2 ELONGATION [%] 83,7 83,7 112,0 121,3 119,5 92,7 93,0 98,7 101,4 101,4 50,9 49,7 56,4 68,8 60,9 std 18,8 13,1 13,1 8,5 16,3 23,0 23,7 17,4 18,4 10,7 11,3 15,2 11,6 17,7 13,6 BONDING INDEX 14,5 17,4 22,5 21,2 21,9 18,7 18,2 21,9 18,9 19,3 10,2 11,7 13,1 12,7 14,0 Table 3: Mechanical properties of non-woven of fibres comprising composition 3 (comparative) SPINNINGTEMP [°C] 260 °C - MF 35 265 °C - MF 47 270 °C - MF 52 CODE 13 E 2 13 E 3 13 E 4 13 E 5 13 E 6 14 E 2 14 E 3 14E 4 14 E 5 14 E 6 15 E 2 15 E 3 15 E 4 15 E 5 15 E 6 CALENDER TEMP. [°C ] 140 143 146 149 152 140 143 146 149 152 140 143 146 149 152 BASIC WEIGHT [g/m2] 21,2 19,0 23,4 21,3 22,5 20,6 16,6 20,0 22,2 22,8 18,4 19,9 23,2 23,1 21,8 MACHINE DIRECTION MAX. FORCE [N] 25,3 35,7 39,5 43,1 41,8 46,3 45,7 44,2 49,3 47,5 30,5 41,6 40,2 27,6 35,6 TENACITY calo/20g/m2 [N/5cm] 23,9 37,6 33,8 40,4 37,1 45,0 55,0 44,2 44,4 41,7 33,1 41,8 34,7 23,9 32,7 std 1,2 1,5 2,9 2,5 2,5 2,4 2,3 3,3 6,5 9,6 3,8 3,4 4,3 3,9 3,3 ELONGATION [%] 15,7 36,5 29,1 34,9 31,6 44,5 54,3 49,4 38,6 39,5 26,5 40,8 30,3 14,8 20,6 std 1,7 2,5 4,4 5,2 4,6 3,7 7,0 9,6 5,6 9,6 5,4 6,8 9,0 3,9 3,8 BASIC WEIGHT [g/m2] 21,2 19,0 23,4 21,3 22,5 20,6 16,6 20,0 22,2 22,8 18,4 19,9 23,2 23,1 21,8 CROSS DIRECTION MAX. FORCE [N ] 2,1 3,3 3,8 4,9 6,8 5,7 7,3 7,5 9,6 10,1 3,9 6,8 6,3 7,0 6,8 TENACITY calc/20g/m3 [N/5cm] 2,0 3,5 3,2 4,6 6,0 5,5 8,8 7,5 8,6 8.8 4,3 6,8 5,5 6,1 6,2 std 0,2 0,2 0,2 0,2 0,4 0,8 0,8 0,4 0,9 0,6 0,7 0,7 1,0 0,9 1,0 ELONGATION [%] 43,6 77,7 72,5 91,8 100,5 89,9 110,8 114,9 113,2 117,5 64,0 83,4 80,0 82,2 80,0 std 5,4 8,6 6,6 7,3 9,0 5,4 16,5 11,5 6,7 13,9 11,7 9,9 15,5 13,5 16,4 BONDING INDEX 6,9 11,5 10,5 13,7 14,9 15,8 22,0 18,2 19,6 19,2 11,9 16,9 13,8 12,0 14,3 Table 4: Bonding index of non-wovens produced with fibres comprising compositions 1, 2 and 3 (comparative). Bonding index of non-wovens produced from fibres comprising composition 1 spinning temperature (°C) calander temperature (°C) 249 255 260 265 140 5.5 18.2 19.2 19.3 143 7 19.5 20.5 20.6 146 9.9 23.7 23.9 23.6 149 10.4 20.6 21 20.6 152 16 20.1 22.1 19.6 Bonding index of non-wovens produced from fibres comprising composition 2 spinning temperature (°C) calander temperature (°C) 260 265 270 140 14.5 18.7 10.2 143 17.4 18.2 11.7 146 22.5 21.9 13.1 149 21.2 18.9 12.7 152 21.9 19.3 14 Bonding index of non-wovens produced from fibres comprising composition 3 (comparative) calander temperature (°C) 260 265 270 140 6.9 15.8 11.9 143 11.5 22 16.9 146 10.5 18.2 13.8 149 13.7 19.6 12 152 14.9 19.2 14.3
Claims (20)
- A non-woven produced by bonding a web formed by propylene polymer fibres with improved thermo bonding properties characterized in that the propylene polymer fibres comprise- a lactone of the furan-2-one type in an amount of 200 ppm or less,- a phosphite compound, and- a UV-stabilizer,wherein the sum of the amounts of said lactone, said phosphite compound and said UV-stabilizer is 700 ppm or less.
- A non-woven according to claim 1 characterized in that said lactone is of the benzofuran-2-one type.
- A non-woven according to claim 2 characterized in that said lactone is of the benzofuran-3-phenyl-2-one type.
- A non-woven according to claim 3 characterized in that said lactone comprises benzofuran-3-phenyl-2-one or an alkyl-substituted derivate thereof or a mixture of any of such compounds.
- A non-woven according to claim 4 characterized in that said lactone comprises 5,7-di-tert-butyl-benzofuran-3-phenyl-2-one or a methyl-substituted derivate thereof or a mixture of any of such compounds.
- A non-woven according to any of the preceding claims characterized in that the propylene polymer fibres are essentially free of phenols.
- A non-woven according to any of the preceding claims characterized in that the propylene polymer fibres comprise staple fibres or continuous filaments.
- A non-woven according to any of the preceding claims characterized in that the propylene polymer fibres comprise staple fibres.
- A process for the production of a non-woven characterized in that it comprises thermo bonding of a web formed by propylene polymer fibres with improved thermo bonding properties wherein to a propylene polymer before spinning of the fibres is added- a lactone of the furan-2-one type in an amount of 200 ppm or less- a phosphite compound, and- a UV-stabilizer,wherein the sum of the amounts of said lactone, said phosphite compound and said UV-stabilizer is 700 ppm or less.
- A process according to claim 9 characterized in that said lactone is of the benzofuran-2-one type.
- A process according to claim 10 characterized in that said lactone is of the benzofuran-3-phenyl-2-one type.
- A process according to claim 11 characterized in that said lactone comprises benzofuran-3-phenyl-2-one or an alkyl-substituted derivate thereof or a mixture of any of such compounds.
- A process according to claim 12 characterized in that said lactone comprises 5,7-di-tert-butyl-benzofuran-3-phenyl-2-one or a methyl-substituted derivate thereof or a mixture of any of such compounds.
- A process according to any of claims 9 to 13 characterized in that essentially no phenols are added to the propylene polymer.
- A process according to any of claims 9 to 14 characterized in that the spinning temperature is from 220 to 300° C.
- A process according to claim 15 characterized in that the spinning temperature is from 245 to 270° C.
- A process according to any of claims 9 to 16 characterized in that said web is thermo bonded at a temperature of from 140 to 155 °C.
- A non-woven characterized in that it is obtainable by a process according to any of claims 9 to 17.
- Use of a propylene polymer composition for the production of a non-woven by thermo bonding of a web of propylene polymer fibres characterized in that said propylene polymer composition comprises- a lactone of the furan-2-one type in an amount of 200 ppm or less,- a phosphite compound, and- a UV-stabilizer,wherein the sum of the amounts of said lactone, said phosphite compound and said UV-stabilizer is 700 ppm or less.
- Use according to claim 19 characterized in that said propylene polymer fibres comprise staple fibres.
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT01112487T ATE339537T1 (en) | 2001-05-22 | 2001-05-22 | FIBER FLEECE |
| DK01112487T DK1260618T3 (en) | 2001-05-22 | 2001-05-22 | Non-woven fabric |
| DE60123022T DE60123022T2 (en) | 2001-05-22 | 2001-05-22 | non-woven fabric |
| EP01112487A EP1260618B1 (en) | 2001-05-22 | 2001-05-22 | Non-woven material |
| PCT/EP2002/005616 WO2002095095A2 (en) | 2001-05-22 | 2002-05-22 | A nonwoven formed by bonding of propylene polymer fibres with bonding properties |
| AU2002339520A AU2002339520A1 (en) | 2001-05-22 | 2002-05-22 | A nonwoven formed by bonding of propylene polymer fibres with bonding properties |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01112487A EP1260618B1 (en) | 2001-05-22 | 2001-05-22 | Non-woven material |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1260618A1 EP1260618A1 (en) | 2002-11-27 |
| EP1260618B1 true EP1260618B1 (en) | 2006-09-13 |
Family
ID=8177511
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01112487A Expired - Lifetime EP1260618B1 (en) | 2001-05-22 | 2001-05-22 | Non-woven material |
Country Status (6)
| Country | Link |
|---|---|
| EP (1) | EP1260618B1 (en) |
| AT (1) | ATE339537T1 (en) |
| AU (1) | AU2002339520A1 (en) |
| DE (1) | DE60123022T2 (en) |
| DK (1) | DK1260618T3 (en) |
| WO (1) | WO2002095095A2 (en) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1809610A (en) * | 2003-06-19 | 2006-07-26 | 巴塞尔聚烯烃意大利有限责任公司 | Olefin polymers with stabilisers and polyolefin fibres produced therefrom |
| EP1736506A1 (en) * | 2005-06-24 | 2006-12-27 | Borealis Technology Oy | Stabilised polypropylene composition |
| DE102021202102A1 (en) | 2021-03-04 | 2022-09-08 | Fraunhofer-Gesellschaft zur Förderung der angewandten Forschung eingetragener Verein | Use of a stabilizer composition for stabilizing organic materials, stabilizer composition, masterbatch, composition, molding composition of the moldings, method for the oxidative, thermal actinic stabilization of a thermoplastic and use of a composition |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6521681B1 (en) * | 1996-07-05 | 2003-02-18 | Ciba Specialty Chemicals Corporation | Phenol-free stabilization of polyolefin fibres |
| US5834541A (en) * | 1997-05-02 | 1998-11-10 | Montell North America Inc. | Olefin polymer composition having low smoke generation and fiber and film prepared therefrom |
| EP0878567B1 (en) * | 1997-05-14 | 2004-09-29 | Borealis GmbH | Polyolefin fibres and polyolefin yarns and textile materials thereof |
-
2001
- 2001-05-22 AT AT01112487T patent/ATE339537T1/en not_active IP Right Cessation
- 2001-05-22 DE DE60123022T patent/DE60123022T2/en not_active Expired - Fee Related
- 2001-05-22 DK DK01112487T patent/DK1260618T3/en active
- 2001-05-22 EP EP01112487A patent/EP1260618B1/en not_active Expired - Lifetime
-
2002
- 2002-05-22 WO PCT/EP2002/005616 patent/WO2002095095A2/en not_active Ceased
- 2002-05-22 AU AU2002339520A patent/AU2002339520A1/en not_active Abandoned
Also Published As
| Publication number | Publication date |
|---|---|
| WO2002095095A2 (en) | 2002-11-28 |
| DK1260618T3 (en) | 2007-01-22 |
| ATE339537T1 (en) | 2006-10-15 |
| WO2002095095A3 (en) | 2003-02-13 |
| DE60123022T2 (en) | 2007-04-19 |
| EP1260618A1 (en) | 2002-11-27 |
| AU2002339520A1 (en) | 2002-12-03 |
| DE60123022D1 (en) | 2006-10-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5281378A (en) | Process of making high thermal bonding fiber | |
| EP0875530B1 (en) | Olefin polymer composition having low smoke generation and fiber and film prepared therefrom | |
| EP0391438B1 (en) | Thermowelded artikels based on polyolefin fibres | |
| JPS61136533A (en) | Composition | |
| EP0530984B1 (en) | Stabilized polyolefin composition | |
| EP1003811B1 (en) | Olefin polymer composition having low smoke generation and fiber, film and fabric prepared therefrom | |
| DE69621410T2 (en) | Stabilized thermoplastic polymer composition | |
| TW202442862A (en) | Flame retardant composition, flame retardant resin composition and molded product | |
| EP1260618A1 (en) | Propylene polymer fibres with bonding properties | |
| EP0905299B1 (en) | Method for producing spun-bonded materials | |
| EP1736506A1 (en) | Stabilised polypropylene composition | |
| EP1633811B1 (en) | Olefin polymers with stabilisers and polyolefin fibres produced therefrom | |
| KR102708190B1 (en) | Polyethylene resin composition for conjugate spinning fibers with excellent spinning property | |
| US20060128849A1 (en) | Olefin polymers with stabilisers and polyolefin fibres produced therefrom | |
| US5278209A (en) | Thermooxidative stabilization of polyolefins with an oxo-piperazinyl-triazine and a phosphorous acid ester | |
| AU762445B2 (en) | Method for producing spun-bonded materials with improved tensile strength | |
| WO2001044362A1 (en) | Olefin polymer composition having low smoke generation and fiber, film and fabric prepared therefrom | |
| JPH10183423A (en) | Polypropylene resin composition for fiber and use thereof | |
| AU630179B2 (en) | Polyolefins suitable for spinning and thermoweldable fibers obtained from them | |
| HK1008747B (en) | Thermowelded articles based on polyolefin fibres | |
| MXPA98007841A (en) | Method to produce agglomerated materials by yarn with better resistance to tracc |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20010522 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17Q | First examination report despatched |
Effective date: 20040804 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B32B 5/00 20060101ALI20060418BHEP Ipc: D04H 1/42 20060101AFI20060418BHEP Ipc: D01F 1/10 20060101ALI20060418BHEP Ipc: D01F 6/06 20060101ALI20060418BHEP |
|
| RTI1 | Title (correction) |
Free format text: NON-WOVEN MATERIAL |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20060913 Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60123022 Country of ref document: DE Date of ref document: 20061026 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061213 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061224 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070226 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| EN | Fr: translation not filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20070614 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20070522 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070518 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061214 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070522 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070522 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20080523 Year of fee payment: 8 Ref country code: DK Payment date: 20080509 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20080523 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070522 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060913 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090522 |