EP1253010B1 - Thermal transfer printing apparatus for marking zip fastener - Google Patents
Thermal transfer printing apparatus for marking zip fastener Download PDFInfo
- Publication number
- EP1253010B1 EP1253010B1 EP01303708A EP01303708A EP1253010B1 EP 1253010 B1 EP1253010 B1 EP 1253010B1 EP 01303708 A EP01303708 A EP 01303708A EP 01303708 A EP01303708 A EP 01303708A EP 1253010 B1 EP1253010 B1 EP 1253010B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- chain
- tape
- printing apparatus
- printer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000010023 transfer printing Methods 0.000 title abstract description 4
- 238000007639 printing Methods 0.000 claims abstract description 32
- 230000008878 coupling Effects 0.000 claims abstract description 9
- 238000010168 coupling process Methods 0.000 claims abstract description 9
- 238000005859 coupling reaction Methods 0.000 claims abstract description 9
- 238000000034 method Methods 0.000 claims description 19
- 239000000463 material Substances 0.000 description 13
- 239000000976 ink Substances 0.000 description 9
- 239000011888 foil Substances 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 4
- 239000003086 colorant Substances 0.000 description 3
- 238000010586 diagram Methods 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 238000005304 joining Methods 0.000 description 2
- 238000007789 sealing Methods 0.000 description 2
- 239000000919 ceramic Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 238000004043 dyeing Methods 0.000 description 1
- 239000004744 fabric Substances 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- 229920006255 plastic film Polymers 0.000 description 1
- 229920000728 polyester Polymers 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000004080 punching Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 239000002904 solvent Substances 0.000 description 1
- 239000004753 textile Substances 0.000 description 1
- 230000001960 triggered effect Effects 0.000 description 1
Images

Classifications
-
- A—HUMAN NECESSITIES
- A44—HABERDASHERY; JEWELLERY
- A44B—BUTTONS, PINS, BUCKLES, SLIDE FASTENERS, OR THE LIKE
- A44B19/00—Slide fasteners
- A44B19/42—Making by processes not fully provided for in one other class, e.g. B21D53/50, B21F45/18, B22D17/16, B29D5/00
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41J—TYPEWRITERS; SELECTIVE PRINTING MECHANISMS, i.e. MECHANISMS PRINTING OTHERWISE THAN FROM A FORME; CORRECTION OF TYPOGRAPHICAL ERRORS
- B41J3/00—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed
- B41J3/407—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed for marking on special material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41J—TYPEWRITERS; SELECTIVE PRINTING MECHANISMS, i.e. MECHANISMS PRINTING OTHERWISE THAN FROM A FORME; CORRECTION OF TYPOGRAPHICAL ERRORS
- B41J3/00—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed
- B41J3/60—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed for printing on both faces of the printing material
Definitions
- This invention relates to an apparatus and a method for marking zip fasteners, and in particular to a thermal transfer contact system for automatically marking zip fasteners.
- Zip fasteners are commonly used for joining together two edges of material. They may be used for providing a closable slit in a unit e.g. as in a dress zip, or they may be used for joining two separate pieces of material together. They are widely used in a upholstery, clothing etc., with almost any type of material. In many situations, a zip fastener will be used to join together two edges of patterned material. A particular example is the manufacture of car seat covers. In this situation, it is important that the pattern on the two edges of material matches.
- a conventional zip fastener has two stringers which are formed from a plurality of coupling elements located on an edge of a tape. The edges of material to be joined are attached to the respective tape and the zip fastener is closed by engaging the coupling elements with a slider. In many situations, it is not practical to attach the material when the zip fastener is closed. Therefore, the zip fastener stringers need to be marked so that the pattern on the edges of the material can be matched with the corresponding position on the stringers.
- a past method of doing this has been to mark the tapes of the zip fastener stringers manually, for example with a pen.
- this method has many disadvantages, in addition to being extremely time consuming and costly. For example, during handling of the stringers, the pen mark can rub off. Also, the tape must be marked on its upper and lower surface. It is awkward to accurately align pen marks on both of these surfaces.
- Another method has been to use alignment marks in the zip-fastener stringer tapes consisting of pairs of open holes.
- the tape of each stringer has a hole at the same positions along the length of the stringers, allowing accurate alignment from either side.
- the holes are punched between the line of attachment of the material and the coupling elements so that the strength of the zip fastener is not weakened.
- the pins used to punch the holes are heated, sealing the walls of the hole. This works well for a polyester type material, although for other materials, a more complicated and more expensive sealing technique may be required.
- a major disadvantage of the hole punching method is that it is time consuming and therefore expensive to punch the holes. Except for particularly long zip fasteners, only a single alignment hole is generally provided, about halfway along the length of the zip fastener.
- the present invention overcomes these problems by providing an apparatus and a method to create alignment marks preferably on both sides of a zip fastener stringer by printing, particularly thermal transfer printing.
- Multiple alignment marks can easily be made along the length of the stringers, so that the material can be matched at more than one point. This is particularly important for long zip fasteners which are used in car seat manufacture.
- the alignment marks may be regularly or irregularly spaced, which may be of use for attaching to material with a more complex pattern or shape, for example. Multiple types of markings may be used, and markings can be accurately aligned on the upper and lower surfaces. Markings can be made using a choice of colours of ink, or using more than one colour of ink. Lengths of chain which have been previously dyed in different colours may be marked.
- Thermal transfer contact systems provide a simple, economical and clean method of printing on layers of fabric, and on many consumer items utilising brightly coloured designs, such as ceramic mugs.
- none of these currently known machines are suited to printing on zip fasteners.
- a printing machine In order to automatically print markings on a zip fastener, a printing machine must be able to take account of the width of the zip fastener chain, and it must be able to automatically deal with both continuous chain and gapped chain, taking account of the spacings between different lengths of gapped chain. It must be able to print on both the front and the back surfaces of zipper chains.
- Thermal transfer printing technology is suitable for printing simple codes or marks onto a flat surface such as plastic film, cases or textile tapes. It ensures good and regular print quality. It is particularly suitable when the code to be printed is short and does not change often. Due to the fact that thermal contact printers use non solvent-based solid inks, ribbons or dry inks, this technology is environmentally friendly.
- DE-A-3825712 and EP-A-414553 show apparatus for marking the stringer tape before elements are attached to the tape to assist with manufacture of the zip fastener.
- EP-A-458220 describes a method of marking the tape to determine when to change the style of the top and bottom stops to be attached at the required location on a continuous chain.
- EP-A-947340 shows a thermal printer for printing onto both sides of therms paper.
- the present invention provides a printing apparatus for marking a zip fastener stringer, as set forth in the accompanying claim 1, and a method of automatically marking a zip fastener stringer as set forth in claim 12.
- the printing means is adapted to print on both tapes of the chain.
- the measuring means comprises a rotary shaft encoder and the feeding means comprises a feed motor.
- the printing apparatus further comprises support means for supporting the chain, allowing gapped chain to be fed through the system, end detector means such as a space detector, for detecting the gap.
- the printing apparatus has a second print head, and the two print heads are positioned such that in use, one print head print onto a first surface of the chain, and the second print head prints onto the reverse surface of the chain.
- the design of the mark to be printed can be manually changed, and the shape of the print heads is adapted to allow printing to the stringers of a zip fastener with a slider.
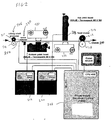
- Figure 1 shows three separate lengths of zip fastener chain 150, 160, 170.
- Each zip fastener chain has two stringers 103 and 105, and each stringer 103, 105 is made up of a tape 107, 109 with a multiple of coupling elements 111, 113 on the edge of the tape 107, 109.
- the elements may be discrete elements or formed by a continuous moulding or helically wound filament as is well known in the art.
- a length of zip fastener chain is made into a zip fastener by removing end fastening elements, replacing them with stops, and adding a slider.
- two tapes are formed and then joined to form a chain which can then be processed further, for example by dyeing, and then shipping. Gaps may be formed in the elements along the chain to indicate start and finish points of individual zip fasteners, for example by cutting away the elements.
- the zip fastener chains of figure 1 show three different possibilities for marking.
- the stringers are symmetrically marked, with level sets of markings 115 spaced at a pre-set interval. Markings are considered level when a line between the markings on each stringer is substantially perpendicular to the direction of closure of the zip fastener.
- an asymmetric marking pattern is shown by markings 117 on stringer 103 being at a different spacing to markings 119 on stringer 105.
- markings 121 on the under side of stringer 105 are aligned with markings 123 on the upper side of stringer 103.
- Figure 2 shows a schematic diagram of a preferred embodiment of the invention.
- Zip fastener chain 200 is fed between two rollers 202, 204 of a rotary shaft encoder 206.
- the rotary shaft encoder 206 sends a signal to a controller 208, indicating the length of chain 200 which has passed through the rollers 202, 204.
- the chain 200 then passes through two sets of print heads.
- a bottom print head 210 prints on the underside of the chain, and a top print head 212 prints on the upper side of the chain 200.
- a feed motor 214 provides the driving force via the rollers 216, 218 to pull the chain 200 through the system.
- the distance between the print heads of the printers 210, 212 is known, and the distance from the rotary encoder 206, and hence the respective printer is triggered by the controller after a calculated length of chain has passed through the rotary encoder 206.
- the top and bottom printers are controlled via two compact control units 220, 222. Suitable control units would be Imaje: 1 Termopack 50 V S3 and 1 Termopack 50 H S3. These are connected to the controller 208. A control panel is provided on the controller 208. Chain guides 230, 232 are used to guide the chain 200 through the system, and into the correct position between the print heads. By changing the chain guides 230, 232, different sizes or widths of chain can be accommodated.
- the printer preferably prints a line or other marking extending in from the outer edge of the tape 107, 109 and may be adjustable to print different lengths. An achievable print head marking speed is 150 cycles per minute. Several ribbon colours are possible, and various types of mark shape are possible. The tolerance of positioning of a mark of 1mm is possible.
- the print head design may allow for the printer to be set to print on one or both sides of the elements of the chain, that is on one or both tapes 107, 109 ( Figure 1). Alternatively, two printers could be provided for printing on respective tapes 107, 109.
- the rotary encoder controls the marking by measuring the passage of the chain.
- the start point of the elements can be detected by a space sensor 240 such as a photocell or a mechanical detector, and the controller then triggers the printers 210, 212 at pre-determined distances from the start point.
- the space sensor is preferably positioned downstream of the rotary encoder 206.
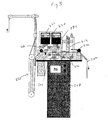
- Figure 3 shows a sectional view of the printing machine.
- the chain is guided and aligned through a tensioner 250 before entering the rotary shaft encoder 206.
- any stretching of the chain 200 between the encoder 206 and the motor 214 can be controlled, to ensure accurate positioning of the markings.
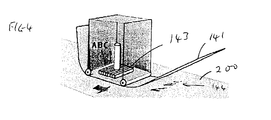
- Figure 4 shows the construction of one of the print heads.
- the print head is fitted with rollers which guide an ink foil 141 below a hot press 143.
- the ink foil 141 enters the print head via a first roller, and leaves via a second roller.
- the zip fastener chain 100 is guided below the print head.
- An image 144 is transferred from the ink foil to the chain 200, by the hot press 143 moving towards the chain, and pressing the ink foil 144 against the chain 100.
- markings can also be printed on the tapes 107, 109 at irregular intervals, such as 10cm, 20 cm, 45 cm from a start point, to suit particular user requirements.
Landscapes
- Electronic Switches (AREA)
- Printers Characterized By Their Purpose (AREA)
- Slide Fasteners (AREA)
- Ink Jet (AREA)
- Accessory Devices And Overall Control Thereof (AREA)
- Impression-Transfer Materials And Handling Thereof (AREA)
- Thermal Transfer Or Thermal Recording In General (AREA)
Abstract
Description
- This invention relates to an apparatus and a method for marking zip fasteners, and in particular to a thermal transfer contact system for automatically marking zip fasteners.
- Zip fasteners are commonly used for joining together two edges of material. They may be used for providing a closable slit in a unit e.g. as in a dress zip, or they may be used for joining two separate pieces of material together. They are widely used in a upholstery, clothing etc., with almost any type of material. In many situations, a zip fastener will be used to join together two edges of patterned material. A particular example is the manufacture of car seat covers. In this situation, it is important that the pattern on the two edges of material matches.
- Matching two such patterns is an awkward process. A conventional zip fastener has two stringers which are formed from a plurality of coupling elements located on an edge of a tape. The edges of material to be joined are attached to the respective tape and the zip fastener is closed by engaging the coupling elements with a slider. In many situations, it is not practical to attach the material when the zip fastener is closed. Therefore, the zip fastener stringers need to be marked so that the pattern on the edges of the material can be matched with the corresponding position on the stringers.
- A past method of doing this has been to mark the tapes of the zip fastener stringers manually, for example with a pen. However, this method has many disadvantages, in addition to being extremely time consuming and costly. For example, during handling of the stringers, the pen mark can rub off. Also, the tape must be marked on its upper and lower surface. It is awkward to accurately align pen marks on both of these surfaces.
- Another method has been to use alignment marks in the zip-fastener stringer tapes consisting of pairs of open holes. The tape of each stringer has a hole at the same positions along the length of the stringers, allowing accurate alignment from either side. The holes are punched between the line of attachment of the material and the coupling elements so that the strength of the zip fastener is not weakened. To prevent fraying, the pins used to punch the holes are heated, sealing the walls of the hole. This works well for a polyester type material, although for other materials, a more complicated and more expensive sealing technique may be required. A major disadvantage of the hole punching method is that it is time consuming and therefore expensive to punch the holes. Except for particularly long zip fasteners, only a single alignment hole is generally provided, about halfway along the length of the zip fastener.
- The present invention overcomes these problems by providing an apparatus and a method to create alignment marks preferably on both sides of a zip fastener stringer by printing, particularly thermal transfer printing. Multiple alignment marks can easily be made along the length of the stringers, so that the material can be matched at more than one point. This is particularly important for long zip fasteners which are used in car seat manufacture. The alignment marks may be regularly or irregularly spaced, which may be of use for attaching to material with a more complex pattern or shape, for example. Multiple types of markings may be used, and markings can be accurately aligned on the upper and lower surfaces. Markings can be made using a choice of colours of ink, or using more than one colour of ink. Lengths of chain which have been previously dyed in different colours may be marked.
- Thermal transfer contact systems provide a simple, economical and clean method of printing on layers of fabric, and on many consumer items utilising brightly coloured designs, such as ceramic mugs. However, none of these currently known machines are suited to printing on zip fasteners. In order to automatically print markings on a zip fastener, a printing machine must be able to take account of the width of the zip fastener chain, and it must be able to automatically deal with both continuous chain and gapped chain, taking account of the spacings between different lengths of gapped chain. It must be able to print on both the front and the back surfaces of zipper chains.
- Thermal transfer printing technology is suitable for printing simple codes or marks onto a flat surface such as plastic film, cases or textile tapes. It ensures good and regular print quality. It is particularly suitable when the code to be printed is short and does not change often. Due to the fact that thermal contact printers use non solvent-based solid inks, ribbons or dry inks, this technology is environmentally friendly.
- DE-A-3825712 and EP-A-414553 show apparatus for marking the stringer tape before elements are attached to the tape to assist with manufacture of the zip fastener. EP-A-458220 describes a method of marking the tape to determine when to change the style of the top and bottom stops to be attached at the required location on a continuous chain. EP-A-947340 shows a thermal printer for printing onto both sides of therms paper.
- The present invention provides a printing apparatus for marking a zip fastener stringer, as set forth in the accompanying claim 1, and a method of automatically marking a zip fastener stringer as set forth in claim 12.
- Preferable, two tapes are joined to form a chain, and the printing means is adapted to print on both tapes of the chain. Preferably, the measuring means comprises a rotary shaft encoder and the feeding means comprises a feed motor. Preferably, the printing apparatus further comprises support means for supporting the chain, allowing gapped chain to be fed through the system, end detector means such as a space detector, for detecting the gap. Preferably, the printing apparatus has a second print head, and the two print heads are positioned such that in use, one print head print onto a first surface of the chain, and the second print head prints onto the reverse surface of the chain. Preferably the design of the mark to be printed can be manually changed, and the shape of the print heads is adapted to allow printing to the stringers of a zip fastener with a slider.
- The invention will now be described by way of example with reference to the following drawings, in which:-
- Figure 1 shows several lengths of zip fastener chain, each with a different arrangement of alignment markings;
- Figure 2 shows a schematic diagram of a preferred embodiment of the invention;
- Figure 3 shows a side view of a preferred embodiment of the invention, and
- Figure 4 shows an expanded view of a print head
- Figure 1 shows three separate lengths of
zip fastener chain stringers stringer tape coupling elements 111, 113 on the edge of thetape - The zip fastener chains of figure 1 show three different possibilities for marking. In the
first chain 150, the stringers are symmetrically marked, with level sets ofmarkings 115 spaced at a pre-set interval. Markings are considered level when a line between the markings on each stringer is substantially perpendicular to the direction of closure of the zip fastener. In thesecond chain 160, an asymmetric marking pattern is shown by markings 117 onstringer 103 being at a different spacing tomarkings 119 onstringer 105. In thethird chain 170,markings 121 on the under side ofstringer 105 are aligned with markings 123 on the upper side ofstringer 103. - Figure 2 shows a schematic diagram of a preferred embodiment of the invention.
Zip fastener chain 200 is fed between tworollers rotary shaft encoder 206. Therotary shaft encoder 206 sends a signal to acontroller 208, indicating the length ofchain 200 which has passed through therollers chain 200 then passes through two sets of print heads. Abottom print head 210 prints on the underside of the chain, and atop print head 212 prints on the upper side of thechain 200. Afeed motor 214 provides the driving force via therollers 216, 218 to pull thechain 200 through the system. - The distance between the print heads of the
printers rotary encoder 206, and hence the respective printer is triggered by the controller after a calculated length of chain has passed through therotary encoder 206. - The top and bottom printers are controlled via two
compact control units controller 208. A control panel is provided on thecontroller 208. Chain guides 230, 232 are used to guide thechain 200 through the system, and into the correct position between the print heads. By changing the chain guides 230, 232, different sizes or widths of chain can be accommodated. The printer preferably prints a line or other marking extending in from the outer edge of thetape - The print head design may allow for the printer to be set to print on one or both sides of the elements of the chain, that is on one or both
tapes 107, 109 (Figure 1).
Alternatively, two printers could be provided for printing onrespective tapes - For continuous chain, the rotary encoder controls the marking by measuring the passage of the chain. For gapped chain, the start point of the elements can be detected by a
space sensor 240 such as a photocell or a mechanical detector, and the controller then triggers theprinters rotary encoder 206. - Figure 3 shows a sectional view of the printing machine. The chain is guided and aligned through a tensioner 250 before entering the
rotary shaft encoder 206. - By controlling the tension, any stretching of the
chain 200 between theencoder 206 and themotor 214 can be controlled, to ensure accurate positioning of the markings. - Figure 4 shows the construction of one of the print heads. The print head is fitted with rollers which guide an
ink foil 141 below ahot press 143. Theink foil 141 enters the print head via a first roller, and leaves via a second roller. Thezip fastener chain 100 is guided below the print head. Animage 144 is transferred from the ink foil to thechain 200, by thehot press 143 moving towards the chain, and pressing theink foil 144 against thechain 100. - It will be appreciated that other printer types, such as ink jet, might be used, but a thermal printer has been found to be particularly suitable.
- By appropriate programming of the
controller 208, markings can also be printed on thetapes
Claims (18)
- A printing apparatus for marking a zip fastener stringer (103, 105), said stringer (103, 105) comprising a plurality of coupling elements (111, 113) located on an edge of a tape (107, 109),
the said printing apparatus comprising:a printer for printing onto said tape (107, 109);feeding means (214, 216, 218) for feeding said stringer (103, 105) past a print head (210, 212) of the printer;measuring means (206) for measuring the passage of said stringer (103, 105) past the print head (210, 212) and providing an output; andcontrol means (208, 220, 222) coupled to said measuring means (206) and to said printers (210, 212), characterised in that said control means is adapted to control the printer to print onto said tape (107, 109) at different intervals according to the output from the measuring means. - A printing apparatus as claimed in claim 1, characterised in that the measuring means comprises a rotary shaft encoder (206).
- A printing apparatus as claimed in claim 2, characterised in that the feeding means comprises a feed motor (214) which pulls the tape (107, 109) through the encoder(206) and past the print head (210, 212).
- A printing apparatus, as claimed in any one of claims 1 to 3, comprising two print heads (210, 212) positioned such that in use, one print head prints onto a first surface of the tape (107, 109), and the second print head prints onto the reverse surface of the tape (107, 109).
- A printing apparatus as claimed in claim 4, characterised in that the control means (208, 220, 222) is programmable to cause the respective print heads to print at different intervals along the tape (107, 109).
- A printing apparatus, as claimed in any one of claims 1 to 5, characterised in that feeding means is adapted to feed a chain (200) comprising a pair of coupled stringers (107, 109) through the apparatus.
- A printing apparatus, as claimed in claim 6, characterised by further comprising end detector means (240) for detecting a gap in the coupling elements (111, 113) along the chain, (200).
- A printing apparatus as claimed in claim 7, characterised in that the end detector means (240) comprises a space detector.
- A printing apparatus as claimed in claim 6, 7 or 8, characterised in that the control means is adapted to control the printer to print at different intervals on the respective tapes (107, 109) of the chain (200).
- A printing apparatus, as claimed in any one of claims 1 to 9, characterised in that the design of the mark to be printed can be changed.
- A printing apparatus, as claimed in any one of claims 1 to 10, characterised in that the printer (210, 212) is a thermal printer.
- A method of automatically marking a zip fastener stringer (103,105), said stringer (103, 105) comprising a plurality of coupling elements (111, 113) located on an edge of a tape (107, 109), the method comprising the steps of:feeding said stringer past the print head (210, 212) of a printer for printing onto said tape (107, 109);measuring the passage of said stringer (103, 105) past the print head (210,212) of the printer with a measuring means (206) and providing an output from the measuring means to a control means (208, 220, 222), andcharacterised by the control means (208, 220, 222) controlling the printer to print onto said tape (107, 109) at different intervals according to the output from the measuring means (206).
- A method as claimed in claim 12, further characterised in that said printer comprises first and second print heads, and printing onto a first surface of said tape with the first print head and printing onto the reverse surface of said tape with the second print head.
- A method as claimed in claim 13, characterised in that the control means controls the respective print heads to print at different intervals along said tape.
- A method as claimed in any one of claims 12,13 or 14, characterised in that a pair of coupled stringers (107, 109), forming a chain (200), are fed past the print head (s).
- A method as claimed in claim 15, further comprising providing end detector means (240) and detecting a gap in the coupling elements (111, 113) along said chain by means of said end detector means.
- A method as claimed in claim 15 or 16, further comprising printing onto the respective tapes at different intervals along said chain.
- A method as claimed in any one of the preceding claims, wherein the printer is a thermal printer.
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT01303708T ATE353047T1 (en) | 2001-04-24 | 2001-04-24 | HEAT TRANSFER PRINTER FOR MARKING ZIPPERS |
| ES01303708T ES2277894T3 (en) | 2001-04-24 | 2001-04-24 | PRINTING DEVICE BY THERMAL TRANSFER TO MARK A ZIPPER CLOSURE. |
| EP01303708A EP1253010B1 (en) | 2001-04-24 | 2001-04-24 | Thermal transfer printing apparatus for marking zip fastener |
| DK01303708T DK1253010T3 (en) | 2001-04-24 | 2001-04-24 | Thermal transfer printer device to sense a zipper |
| DE60126400T DE60126400T2 (en) | 2001-04-24 | 2001-04-24 | Heat transfer printer for marking zips |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01303708A EP1253010B1 (en) | 2001-04-24 | 2001-04-24 | Thermal transfer printing apparatus for marking zip fastener |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1253010A1 EP1253010A1 (en) | 2002-10-30 |
| EP1253010B1 true EP1253010B1 (en) | 2007-01-31 |
Family
ID=8181919
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01303708A Expired - Lifetime EP1253010B1 (en) | 2001-04-24 | 2001-04-24 | Thermal transfer printing apparatus for marking zip fastener |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1253010B1 (en) |
| AT (1) | ATE353047T1 (en) |
| DE (1) | DE60126400T2 (en) |
| DK (1) | DK1253010T3 (en) |
| ES (1) | ES2277894T3 (en) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2013248801A (en) * | 2012-05-31 | 2013-12-12 | Ykk Corp | Marking device for slide fastener |
| WO2014091557A1 (en) * | 2012-12-11 | 2014-06-19 | Ykk株式会社 | Marking device |
| WO2014091607A1 (en) * | 2012-12-13 | 2014-06-19 | Ykk株式会社 | Fastener chain manufacturing method and slide fastener |
| CN104985731A (en) * | 2015-07-02 | 2015-10-21 | 重庆永钢橡塑有限责任公司 | Equipment for automatic plastic dipping of super-long chain |
| DE112016007084B4 (en) | 2016-07-21 | 2022-08-18 | Ykk Corporation | MARKING DEVICE AND METHOD |
| CN108244772B (en) * | 2016-12-29 | 2020-12-15 | Ykk株式会社 | Marking mechanism, processing device and processing method of zipper chain |
| GB202201201D0 (en) * | 2022-01-31 | 2022-03-16 | Ykk Europe Ltd | Fastener |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2925831A1 (en) * | 1979-06-27 | 1981-01-15 | Prym Werke William | Slide fasteners precision testing system - includes markings showing number of links per division |
| DE8817036U1 (en) * | 1988-07-28 | 1992-01-23 | Opti Patent-, Forschungs- Und Fabrikations-Ag, Riedern-Allmeind | Machine for producing individual zippers from a long zipper chain |
| AU624520B2 (en) * | 1989-07-15 | 1992-06-11 | Ykk Corporation | Method of and apparatus for manufacturing slide fasteners |
| JPH0659247B2 (en) * | 1989-08-23 | 1994-08-10 | 吉田工業株式会社 | Slide fastener manufacturing method |
| JPH0767401B2 (en) * | 1990-05-19 | 1995-07-26 | ワイケイケイ株式会社 | Method of manufacturing slide fastener |
| JPH11286147A (en) * | 1998-04-02 | 1999-10-19 | Nec Yonezawa Ltd | Double-sided printing mechanism |
-
2001
- 2001-04-24 DE DE60126400T patent/DE60126400T2/en not_active Expired - Lifetime
- 2001-04-24 ES ES01303708T patent/ES2277894T3/en not_active Expired - Lifetime
- 2001-04-24 AT AT01303708T patent/ATE353047T1/en not_active IP Right Cessation
- 2001-04-24 EP EP01303708A patent/EP1253010B1/en not_active Expired - Lifetime
- 2001-04-24 DK DK01303708T patent/DK1253010T3/en active
Also Published As
| Publication number | Publication date |
|---|---|
| ES2277894T3 (en) | 2007-08-01 |
| DE60126400T2 (en) | 2007-11-15 |
| DE60126400D1 (en) | 2007-03-22 |
| DK1253010T3 (en) | 2007-03-05 |
| ATE353047T1 (en) | 2007-02-15 |
| EP1253010A1 (en) | 2002-10-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0785079B1 (en) | Thermal transcription printer | |
| JP5355862B2 (en) | Inkjet recording method | |
| US4785750A (en) | Automatic means of accurately detecting and cutting fabric panels | |
| EP1253010A1 (en) | Thermal transfer printing apparatus for marking zip fastener | |
| JPH0839881A (en) | Thermal transfer printer and positioning device in thermal transfer printer | |
| TWI551235B (en) | Chain manufacturing method and zipper | |
| JP2004505802A (en) | Plant for manufacturing printed textile tapes, especially label tapes | |
| US20020084648A1 (en) | Accurate registration for imaging | |
| CN104168794A (en) | Marking device | |
| US20100177143A1 (en) | Method for printing endless printing substrates digitally | |
| KR102762142B1 (en) | Inkjet Printer for Decoration | |
| US20240409274A1 (en) | System and Method for Bag Closure Clip Production | |
| KR20080108979A (en) | Feeding System for Image Former | |
| GB2397277A (en) | Tag printing device including printing, marking and cutting means operable in accordance with the detected position of holes in the tags | |
| DE4023784A1 (en) | METHOD FOR SETTING A COLOR OF A MULTICOLOR RIBBON WITH A THERMAL TRANSFER PRINTER | |
| JPH08152917A (en) | Transfer device | |
| JP2004306476A (en) | Printers and print media | |
| KR200270600Y1 (en) | Cutting apparatus of paper burlap bag | |
| JPS5911278A (en) | Color thermal printer | |
| JP2001145506A (en) | Patterned slide fastener and its manufacturing method | |
| JP4322489B2 (en) | Label continuum | |
| JP2006068984A (en) | Cutting device for transcript | |
| JPH01218878A (en) | Color detection construction for ink sheet | |
| KR20060034657A (en) | Printing apparatus having a substrate fixing means | |
| JPH01152081A (en) | Tag printing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20030417 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17Q | First examination report despatched |
Effective date: 20040812 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60126400 Country of ref document: DE Date of ref document: 20070322 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070430 |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070702 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2277894 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20070430 |
|
| 26N | No opposition filed |
Effective date: 20071101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070430 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070501 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20080430 Year of fee payment: 8 Ref country code: ES Payment date: 20080520 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070424 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070131 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090430 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20090425 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090425 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20140305 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150424 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20200316 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20200312 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20200415 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20200312 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 60126400 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MK Effective date: 20210424 |