EP0976858B1 - Ribbon-like elements for making holding structures for tubular workpieces of elastomer material - Google Patents
Ribbon-like elements for making holding structures for tubular workpieces of elastomer material Download PDFInfo
- Publication number
- EP0976858B1 EP0976858B1 EP98830440A EP98830440A EP0976858B1 EP 0976858 B1 EP0976858 B1 EP 0976858B1 EP 98830440 A EP98830440 A EP 98830440A EP 98830440 A EP98830440 A EP 98830440A EP 0976858 B1 EP0976858 B1 EP 0976858B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- ribbon
- warp threads
- shaped element
- woof
- threads
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 229920001971 elastomer Polymers 0.000 title abstract 2
- 239000000463 material Substances 0.000 title description 2
- 239000000806 elastomer Substances 0.000 title 1
- 238000003466 welding Methods 0.000 claims abstract description 10
- 239000013536 elastomeric material Substances 0.000 claims description 12
- 238000000034 method Methods 0.000 claims description 7
- 230000008569 process Effects 0.000 claims description 7
- 229920002994 synthetic fiber Polymers 0.000 claims description 4
- 239000004677 Nylon Substances 0.000 claims description 2
- 229920001778 nylon Polymers 0.000 claims description 2
- 238000004073 vulcanization Methods 0.000 abstract description 5
- 230000000694 effects Effects 0.000 abstract description 3
- 239000004753 textile Substances 0.000 abstract description 2
- 238000004519 manufacturing process Methods 0.000 description 6
- 230000009471 action Effects 0.000 description 2
- 230000004075 alteration Effects 0.000 description 2
- 230000008878 coupling Effects 0.000 description 2
- 238000010168 coupling process Methods 0.000 description 2
- 238000005859 coupling reaction Methods 0.000 description 2
- 230000003014 reinforcing effect Effects 0.000 description 2
- 230000003068 static effect Effects 0.000 description 2
- 238000002604 ultrasonography Methods 0.000 description 2
- 230000003313 weakening effect Effects 0.000 description 2
- 238000004804 winding Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 230000003116 impacting effect Effects 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 238000009877 rendering Methods 0.000 description 1
- 238000009958 sewing Methods 0.000 description 1
Images
Classifications
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D23/00—General weaving methods not special to the production of any particular woven fabric or the use of any particular loom; Weaves not provided for in any other single group
Definitions
- the present invention relates to a ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material undergoing work processes, comprising the characteristics expressed in the preamble to Claim 1.
- flexible tubular artefacts of the type commonly used to form for instance pressurised hydraulic circuits and the like, normally comprise at least one reinforcing structure made of textile or metallic material embedded in or coated by at least one layer of elastomeric material.
- the tubular artefact normally obtained from a continuous extrusion process, is appropriately conveyed into vulcanisation station wherein the crude elastomeric material applied to the reinforcing structure reticulates while hardening, thereby forming the final product.
- This containment action is particularly important when the tube is in the vulcanisation station, since the crude elastomeric material, being by its nature malleable, presents quite a high degree of softness which increases at the start of the vulcanisation phase because of the heating it undergoes.
- the ribbon-shaped containment structure applied on the tubular artefact thus prevents the crude elastomeric material from decomposing and jeopardising the structural integrity of the artefact itself.
- the ribbon-shaped containment structure comprises a series of ribbon-shaped elements coupled to each other consecutively in correspondence with respective ends mutually overlaid and sown together to guarantee the continuity of the ribbon-shaped structure.
- Each ribbon-shaped element in turn comprises a plurality of warp threads enmeshed with at least one woof thread positioned according to alternate transverse first and second sections arranged consecutively, to form a reticular structure.
- the reticular structure generated by the enmeshing of the warp threads with the sections of woof thread normally presents discontinuous surfaces due to a difference in count existing between the warp threads and the woof threads.
- the warp threads generally present a greater count than the woof thread, for they must directly withstand the traction whereto the ribbon structure is subjected when it is wound around the tubular artefact.
- the count of the warp thread may for instance have a value of the order of 235 dTex, whereas the count of the woof thread can be of 110 dTex.
- a first problem is given by the fact that the seam makes on the crude elastomeric element an impression which alters the structural characteristics of the tubular artefact, thereby lowering its quality and causing it to be downgraded.
- each seam determines a localised weakening of the reticular structure of the ribbon-shaped element generating such structural discontinuities that, in correspondence with the seam areas, the containment structure is more prone to breakages and/or tears in the ribbon-shaped elements themselves.
- the object of the present invention is essentially to overcome the drawbacks of the prior art, by means of a ribbon-shaped element so structured as to allow it to be optimally joined with other identical ribbon-shaped elements, through ultrasonic welding, in such a way that the containment structure withstands traction stresses effectively when being wound around the tubular artefact, and at the same time it avoids altering the structure of the crude elastomeric material with any impressions.
- a further aim of the invention is to reduce the manufacturing costs of the tubular artefacts of the kind described, definitively eliminating the sewing operations mandatorily present in the prior art and reducing the manufacturing costs of the ribbon-shaped elements.
- the number 1 indicates in its entirety a ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material.
- the ribbon-shaped element 1 comprises a plurality of warp threads 2 made of synthetic material interwoven with at least one woof thread 3 made of synthetic material to form therewith a reticular structure 4.
- the woof thread 3 is usually arranged according to consecutive woofs 3a, each formed by a first section 5 and a second section 6 extending transversely to the warp threads 2 according to alternating directions.
- the warp threads 2 are arranged according to a density essentially equal to the density according to which the first 5 and second 6 sections are arranged.
- the density of the warp threads 2 ranges preferably between 30 and 40 threads/cm given that, if warp threads 2 were used with a lesser density than the minimum value indicated above, the ribbon-shaped element would have poor resistance, and hence be quite fragile with respect to static and/or dynamic loads.
- the maximum recommended limit be exceeded one would have a ribbon-shaped element 1 able to withstand static and/or dynamic loads, but also presenting excess material impacting on manufacturing costs as well as the flexibility and handiness of the ribbon-shaped element for purposes of its winding onto the tubular artefact undergoing work processes.
- the warp threads 2 also present the same count as the woof thread 3, thereby rendering the reticular structure 4 of the ribbon-shaped element 1 compact and uniform.
- the count of the warp threads 2, like that of the woof thread 3, preferably ranges from 100 to 250 dTex and it is advisable to use, both as warp and as woof threads, heavy duty 6.6 nylon threads, with breaking limit preferably no lower than 7g/Tex.
- the uniformity of the reticular structure 4 of the ribbon-shaped element 1 confers thereto the possibility of being welded effectively to another identical ribbon-shaped element through ultrasonic welding.
- Ultrasonic welding can be performed positioning one end of a first ribbon-shaped element 1 to overlay one end of a second ribbon-shaped element 1.
- the two ends are pressed against each other with a pre-set pressure and are simultaneously exposed to ultrasonic waves produced by known apparatuses such as sonotrodes.
- the ribbon-shaped element 1 according to the present invention attains the proposed aims.
- the structure of the ribbon-shaped elements described above thanks to the equality in the density and count of the warp and of the woof, entails considerable advantages.
- a homogeneous and uniform structure such as the one obtainable according to the invention allows to optimise the union of the ribbon-shaped elements by means of ultrasound welding.
- the ribbon-shaped element realised according to the invention presents essentially smooth surfaces, free of discontinuities deriving from the enmeshing of warp and woof threads having different counts. This circumstance allows to increase the contact area between the mutual junction surfaces of the ribbon-shaped elements, and to exploit the potential of ultrasonic welding to the utmost.
- the coupling according to the preceding description completely eliminates the structural alterations generated by the seams, obtaining a tough coupling, effectively resistant to stresses, even when the overlay area between the ribbons presents an extremely reduced width.
- This allows considerably to reduce woof density and, above all, warp density, thereby lightening the ribbon-shaped elements, reducing their manufacturing costs and increasing their handiness and flexibility, thus facilitating their winding around the tubular artefacts, unlike prior art ribbons which were over-dimensioned to withstand the localised weakening due to the structural alterations that the seams entailed.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
- Springs (AREA)
- Laminated Bodies (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
Abstract
Description
- The present invention relates to a ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material undergoing work processes, comprising the characteristics expressed in the preamble to Claim 1.
- As is well known, flexible tubular artefacts, of the type commonly used to form for instance pressurised hydraulic circuits and the like, normally comprise at least one reinforcing structure made of textile or metallic material embedded in or coated by at least one layer of elastomeric material.
- The tubular artefact, normally obtained from a continuous extrusion process, is appropriately conveyed into vulcanisation station wherein the crude elastomeric material applied to the reinforcing structure reticulates while hardening, thereby forming the final product.
- Before performing the vulcanisation, onto the tubular artefact is helically wound a ribbon-shaped containment structure whose task is to contain and stabilise the crude elastomeric material during the work processes.
- This containment action is particularly important when the tube is in the vulcanisation station, since the crude elastomeric material, being by its nature malleable, presents quite a high degree of softness which increases at the start of the vulcanisation phase because of the heating it undergoes. The ribbon-shaped containment structure applied on the tubular artefact thus prevents the crude elastomeric material from decomposing and jeopardising the structural integrity of the artefact itself.
- In particular, the ribbon-shaped containment structure comprises a series of ribbon-shaped elements coupled to each other consecutively in correspondence with respective ends mutually overlaid and sown together to guarantee the continuity of the ribbon-shaped structure.
- Each ribbon-shaped element in turn comprises a plurality of warp threads enmeshed with at least one woof thread positioned according to alternate transverse first and second sections arranged consecutively, to form a reticular structure.
- The reticular structure generated by the enmeshing of the warp threads with the sections of woof thread normally presents discontinuous surfaces due to a difference in count existing between the warp threads and the woof threads. The warp threads generally present a greater count than the woof thread, for they must directly withstand the traction whereto the ribbon structure is subjected when it is wound around the tubular artefact.
- The count of the warp thread may for instance have a value of the order of 235 dTex, whereas the count of the woof thread can be of 110 dTex.
- A ribbon shaped element similar to the one cited above is disclosed on the document US 4688598 A.
- The ribbon-shaped elements coupled as stated above by means of appropriate seams effected on the overlaid ends give rise to considerable problems.
- A first problem is given by the fact that the seam makes on the crude elastomeric element an impression which alters the structural characteristics of the tubular artefact, thereby lowering its quality and causing it to be downgraded.
- It should also be considered that each seam determines a localised weakening of the reticular structure of the ribbon-shaped element generating such structural discontinuities that, in correspondence with the seam areas, the containment structure is more prone to breakages and/or tears in the ribbon-shaped elements themselves.
- It should further be noted that the operations whereby a ribbon is joined to the other determine a rise in manufacturing costs, due to the employment of manpower tasked solely with effecting the seams.
- The Applicant has also noted that it is possible to effect the junction of the ribbon-shaped elements by means of ultrasonic welding. Ultrasonic welded ribbon-shaped elements are shown on the documents US 3901749 A and US 5 223 070 A. However state of the art ribbon-shaped elements are not suited to be effectively joined according to the purposes aimed by the invention.
- The object of the present invention is essentially to overcome the drawbacks of the prior art, by means of a ribbon-shaped element so structured as to allow it to be optimally joined with other identical ribbon-shaped elements, through ultrasonic welding, in such a way that the containment structure withstands traction stresses effectively when being wound around the tubular artefact, and at the same time it avoids altering the structure of the crude elastomeric material with any impressions.
- A further aim of the invention is to reduce the manufacturing costs of the tubular artefacts of the kind described, definitively eliminating the sewing operations mandatorily present in the prior art and reducing the manufacturing costs of the ribbon-shaped elements.
- These aims and others besides, which shall become more readily apparent in the course of the present description, are reached by a ribbon-shaped elements for realising structures for the containment of tubular artefacts made of elastomeric material undergoing work processes, comprising the characteristics expressed in the characterising part of Claim 1.
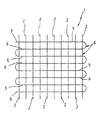
- Additional features and advantages shall become more readily apparent from the detailed description of at least one preferred, but not exclusive, embodiment of a ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material undergoing work processes, according to the present invention. The description shall be made hereafter with reference to the accompanying drawings, provided purely by way of non-limiting indication, whose sole figure shows a structural diagram of a ribbon-shaped element according to the invention.
- With reference to the aforementioned figure, the number 1 indicates in its entirety a ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material.
- The ribbon-shaped element 1 comprises a plurality of
warp threads 2 made of synthetic material interwoven with at least onewoof thread 3 made of synthetic material to form therewith a reticular structure 4. Thewoof thread 3 is usually arranged according to consecutive woofs 3a, each formed by afirst section 5 and asecond section 6 extending transversely to thewarp threads 2 according to alternating directions. - More specifically, the
warp threads 2 are arranged according to a density essentially equal to the density according to which the first 5 and second 6 sections are arranged. The density of thewarp threads 2 ranges preferably between 30 and 40 threads/cm given that, ifwarp threads 2 were used with a lesser density than the minimum value indicated above, the ribbon-shaped element would have poor resistance, and hence be quite fragile with respect to static and/or dynamic loads. On the other hand, should the maximum recommended limit be exceeded, one would have a ribbon-shaped element 1 able to withstand static and/or dynamic loads, but also presenting excess material impacting on manufacturing costs as well as the flexibility and handiness of the ribbon-shaped element for purposes of its winding onto the tubular artefact undergoing work processes. - The
warp threads 2 also present the same count as thewoof thread 3, thereby rendering the reticular structure 4 of the ribbon-shaped element 1 compact and uniform. In particular, the count of thewarp threads 2, like that of thewoof thread 3, preferably ranges from 100 to 250 dTex and it is advisable to use, both as warp and as woof threads, heavy duty 6.6 nylon threads, with breaking limit preferably no lower than 7g/Tex. - The uniformity of the reticular structure 4 of the ribbon-shaped element 1 confers thereto the possibility of being welded effectively to another identical ribbon-shaped element through ultrasonic welding.
- Ultrasonic welding can be performed positioning one end of a first ribbon-shaped element 1 to overlay one end of a second ribbon-shaped element 1. The two ends are pressed against each other with a pre-set pressure and are simultaneously exposed to ultrasonic waves produced by known apparatuses such as sonotrodes.
- During the exposure of the ribbon-shaped elements 1 to the action of the ultrasounds, as an effect of the mechanical vibrations generated thereby, such a quantity of heat develops due to mechanical friction as to induce localised fusion and the consequent welding of the surfaces of the ribbon-shaped element 1 in mutual contact.
- The ribbon-shaped element 1 according to the present invention attains the proposed aims.
- The structure of the ribbon-shaped elements described above, thanks to the equality in the density and count of the warp and of the woof, entails considerable advantages. A homogeneous and uniform structure such as the one obtainable according to the invention allows to optimise the union of the ribbon-shaped elements by means of ultrasound welding. In particular, the ribbon-shaped element realised according to the invention presents essentially smooth surfaces, free of discontinuities deriving from the enmeshing of warp and woof threads having different counts. This circumstance allows to increase the contact area between the mutual junction surfaces of the ribbon-shaped elements, and to exploit the potential of ultrasonic welding to the utmost.
- It should further be considered that the ability to couple the ribbon-shaped elements by means of ultrasonic welds determines a considerable decrease in the manufacturing costs closely linked to the use of manpower tasked solely with effecting the seams.
- The coupling according to the preceding description completely eliminates the structural alterations generated by the seams, obtaining a tough coupling, effectively resistant to stresses, even when the overlay area between the ribbons presents an extremely reduced width. This allows considerably to reduce woof density and, above all, warp density, thereby lightening the ribbon-shaped elements, reducing their manufacturing costs and increasing their handiness and flexibility, thus facilitating their winding around the tubular artefacts, unlike prior art ribbons which were over-dimensioned to withstand the localised weakening due to the structural alterations that the seams entailed.
- It should also be noted that, having eliminated the junction seams between a ribbon-shaped element and the other and having minimised the width of the overlapping areas therebetween, the containment structures thus composed leave no impressions on the crude elastomeric material.
Claims (2)
- Ribbon-shaped element for realising structures for the containment of tubular artefacts made of elastomeric material undergoing work processes, comprising:characterised in that:a plurality of warp threads (2) made of synthetic material;at least one woof thread (3) made of synthetic material and presenting first sections (5) and second sections (6) alternatively consecutive and arranged transversely with respect to the warp threads (2) engaging the latter to form an interwoven structure,the warp threads (2) present the same count as said at least one woof thread (3), the count of the warp threads (2) and of said at least one woof thread (3) ranges between 100 and 250 dTex;the warp threads (2) are arranged according to a density that is equal to the density according to which the first (5) and second (6) sections of said at least one warp thread (3) are distributed;the density of the warp threads (2) ranges between 30 and 40 threads per cm;said warp threads (2) and said at least one woof thread (3) are made of heavy-duty 6.6 nylon with breaking limit exceeding 7g/dTex;said ribbon-shaped element is suitable to be coupled with an identical ribbon-shaped element (1) by means of ultrasonic welding effected on respective'overlaid ends
- Ribbon-shaped containment structure realised from a plurality of ribbon-shaped elements according to claim 1 consecutively coupled by means of ultrasonic welding effected on respective mutually overlaid ends.
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP98830440A EP0976858B1 (en) | 1998-07-21 | 1998-07-21 | Ribbon-like elements for making holding structures for tubular workpieces of elastomer material |
| DE69801993T DE69801993T2 (en) | 1998-07-21 | 1998-07-21 | Ribbon elements for the production of a support structure for tubular elastomeric workpieces |
| AT98830440T ATE206775T1 (en) | 1998-07-21 | 1998-07-21 | FLAT BAND ELEMENTS FOR PRODUCING A HOLDER STRUCTURE FOR TUBULAR ELASTOMER WORKPIECES |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP98830440A EP0976858B1 (en) | 1998-07-21 | 1998-07-21 | Ribbon-like elements for making holding structures for tubular workpieces of elastomer material |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0976858A1 EP0976858A1 (en) | 2000-02-02 |
| EP0976858B1 true EP0976858B1 (en) | 2001-10-10 |
Family
ID=8236722
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98830440A Expired - Lifetime EP0976858B1 (en) | 1998-07-21 | 1998-07-21 | Ribbon-like elements for making holding structures for tubular workpieces of elastomer material |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0976858B1 (en) |
| AT (1) | ATE206775T1 (en) |
| DE (1) | DE69801993T2 (en) |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5413149A (en) * | 1991-11-05 | 1995-05-09 | The Bentley-Harris Manufacturing Company | Shaped fabric products and methods of making same |
-
1998
- 1998-07-21 EP EP98830440A patent/EP0976858B1/en not_active Expired - Lifetime
- 1998-07-21 DE DE69801993T patent/DE69801993T2/en not_active Expired - Fee Related
- 1998-07-21 AT AT98830440T patent/ATE206775T1/en not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| DE69801993D1 (en) | 2001-11-15 |
| ATE206775T1 (en) | 2001-10-15 |
| EP0976858A1 (en) | 2000-02-02 |
| DE69801993T2 (en) | 2002-04-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR100502762B1 (en) | Belt reinforcing material and belt constructed therewith | |
| US5026595A (en) | Woven gap filler for use in the lay-up of composite plastic structural units | |
| EP1992837B1 (en) | Method of producing a power transmission belt in an upright manner | |
| KR0139081B1 (en) | Stabilized fabrics and reinforcements comprising them | |
| US4265627A (en) | Power transmission belt | |
| CN111319913B (en) | Belt as a continuous traction means and method for manufacturing such a belt | |
| US5206079A (en) | Taking-up liners for unvulcanized rubber members | |
| EP0976858A1 (en) | Ribbon-like elements for making holding structures for tubular workpieces of elastomer material | |
| US5690528A (en) | Release liner and method of using same | |
| US532902A (en) | Textile fabric for tubing-envelopes | |
| GB2104996A (en) | Hose | |
| EP1156252B1 (en) | Flexible hose, in particular for watering applications | |
| HUP0203329A2 (en) | Textile material in sheet form for technical uses | |
| JPH02243407A (en) | Wire carrier and its producing method | |
| EP0393083B1 (en) | A flexible reinforced polymeric material and a method of forming such a material | |
| US4741924A (en) | Method of making a polymeric coated fabric layer | |
| US20010031592A1 (en) | Wning cloth and process for producing same | |
| JP3709710B2 (en) | Refrigerant transport hose and manufacturing method thereof | |
| US489714A (en) | Bicycle and other tubing | |
| US4369941A (en) | Reinforcing strip | |
| JPH0243409A (en) | Net for civil engineering work and its laying method | |
| GB2199629A (en) | Kink resistant hose | |
| JP2000192388A (en) | Net for paper manufacturing use | |
| EP1630451A2 (en) | Power transmission belt using stabilized open mesh textile material in overcord for enhanced rubber penetration | |
| JPS6139140Y2 (en) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19990503 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT DE ES FR GB IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17Q | First examination report despatched |
Effective date: 20000523 |
|
| AKX | Designation fees paid |
Free format text: AT DE ES FR GB IT |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: NASTRIFICIO ASSI S.R.L |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT DE ES FR GB IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20011010 |
|
| REF | Corresponds to: |
Ref document number: 206775 Country of ref document: AT Date of ref document: 20011015 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 69801993 Country of ref document: DE Date of ref document: 20011115 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020721 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20020721 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20080724 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20080725 Year of fee payment: 11 Ref country code: FR Payment date: 20080804 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100202 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090721 |