EP0320548B1 - Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties - Google Patents
Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties Download PDFInfo
- Publication number
- EP0320548B1 EP0320548B1 EP19870311114 EP87311114A EP0320548B1 EP 0320548 B1 EP0320548 B1 EP 0320548B1 EP 19870311114 EP19870311114 EP 19870311114 EP 87311114 A EP87311114 A EP 87311114A EP 0320548 B1 EP0320548 B1 EP 0320548B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- max
- duplex stainless
- stainless steel
- nickel
- composition
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 229910001039 duplex stainless steel Inorganic materials 0.000 title claims description 13
- 238000004519 manufacturing process Methods 0.000 title description 2
- 239000000956 alloy Substances 0.000 claims description 46
- 229910045601 alloy Inorganic materials 0.000 claims description 44
- 239000000203 mixture Substances 0.000 claims description 36
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 35
- 229910000859 α-Fe Inorganic materials 0.000 claims description 19
- 229910052759 nickel Inorganic materials 0.000 claims description 16
- 239000011651 chromium Substances 0.000 claims description 15
- 238000012360 testing method Methods 0.000 claims description 14
- 229910052748 manganese Inorganic materials 0.000 claims description 13
- 239000011572 manganese Substances 0.000 claims description 13
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 claims description 12
- 229910052799 carbon Inorganic materials 0.000 claims description 12
- 229910052750 molybdenum Inorganic materials 0.000 claims description 12
- 229910052757 nitrogen Inorganic materials 0.000 claims description 12
- 229910052710 silicon Inorganic materials 0.000 claims description 12
- 229910052804 chromium Inorganic materials 0.000 claims description 11
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims description 10
- 238000000034 method Methods 0.000 claims description 7
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 6
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims description 6
- PWHULOQIROXLJO-UHFFFAOYSA-N Manganese Chemical compound [Mn] PWHULOQIROXLJO-UHFFFAOYSA-N 0.000 claims description 6
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 claims description 6
- OAICVXFJPJFONN-UHFFFAOYSA-N Phosphorus Chemical compound [P] OAICVXFJPJFONN-UHFFFAOYSA-N 0.000 claims description 6
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 claims description 6
- NINIDFKCEFEMDL-UHFFFAOYSA-N Sulfur Chemical compound [S] NINIDFKCEFEMDL-UHFFFAOYSA-N 0.000 claims description 6
- 229910001566 austenite Inorganic materials 0.000 claims description 6
- 238000010438 heat treatment Methods 0.000 claims description 6
- 239000011733 molybdenum Substances 0.000 claims description 6
- 229910052698 phosphorus Inorganic materials 0.000 claims description 6
- 239000011574 phosphorus Substances 0.000 claims description 6
- 239000010703 silicon Substances 0.000 claims description 6
- 229910052717 sulfur Inorganic materials 0.000 claims description 6
- 239000011593 sulfur Substances 0.000 claims description 6
- 238000001816 cooling Methods 0.000 claims description 4
- 229910001262 Ferralium Inorganic materials 0.000 claims description 3
- 229910052742 iron Inorganic materials 0.000 claims description 3
- 229910000593 SAF 2205 Inorganic materials 0.000 claims 1
- 229910000831 Steel Inorganic materials 0.000 claims 1
- 239000012535 impurity Substances 0.000 claims 1
- 239000011159 matrix material Substances 0.000 claims 1
- 239000010959 steel Substances 0.000 claims 1
- 239000000463 material Substances 0.000 description 32
- 229910001220 stainless steel Inorganic materials 0.000 description 26
- 230000007797 corrosion Effects 0.000 description 15
- 238000005260 corrosion Methods 0.000 description 15
- 238000005336 cracking Methods 0.000 description 7
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 description 6
- RWSOTUBLDIXVET-UHFFFAOYSA-N Dihydrogen sulfide Chemical group S RWSOTUBLDIXVET-UHFFFAOYSA-N 0.000 description 5
- 239000000047 product Substances 0.000 description 5
- 229910000037 hydrogen sulfide Inorganic materials 0.000 description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- QTBSBXVTEAMEQO-UHFFFAOYSA-N Acetic acid Chemical compound CC(O)=O QTBSBXVTEAMEQO-UHFFFAOYSA-N 0.000 description 3
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 3
- 150000001805 chlorine compounds Chemical class 0.000 description 3
- 238000010586 diagram Methods 0.000 description 3
- 239000011780 sodium chloride Substances 0.000 description 3
- 238000003466 welding Methods 0.000 description 3
- CURLTUGMZLYLDI-UHFFFAOYSA-N Carbon dioxide Chemical compound O=C=O CURLTUGMZLYLDI-UHFFFAOYSA-N 0.000 description 2
- VEXZGXHMUGYJMC-UHFFFAOYSA-M Chloride anion Chemical compound [Cl-] VEXZGXHMUGYJMC-UHFFFAOYSA-M 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 238000005266 casting Methods 0.000 description 2
- 230000002939 deleterious effect Effects 0.000 description 2
- 230000006698 induction Effects 0.000 description 2
- 239000002244 precipitate Substances 0.000 description 2
- 238000010791 quenching Methods 0.000 description 2
- 238000010998 test method Methods 0.000 description 2
- IRLPACMLTUPBCL-KQYNXXCUSA-N 5'-adenylyl sulfate Chemical compound C1=NC=2C(N)=NC=NC=2N1[C@@H]1O[C@H](COP(O)(=O)OS(O)(=O)=O)[C@@H](O)[C@H]1O IRLPACMLTUPBCL-KQYNXXCUSA-N 0.000 description 1
- UCKMPCXJQFINFW-UHFFFAOYSA-N Sulphide Chemical compound [S-2] UCKMPCXJQFINFW-UHFFFAOYSA-N 0.000 description 1
- 238000005275 alloying Methods 0.000 description 1
- 239000010953 base metal Substances 0.000 description 1
- 239000001569 carbon dioxide Substances 0.000 description 1
- 229910002092 carbon dioxide Inorganic materials 0.000 description 1
- 238000005352 clarification Methods 0.000 description 1
- 230000003749 cleanliness Effects 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000006056 electrooxidation reaction Methods 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 239000007789 gas Substances 0.000 description 1
- 230000014509 gene expression Effects 0.000 description 1
- 230000002401 inhibitory effect Effects 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 238000010309 melting process Methods 0.000 description 1
- 239000003921 oil Substances 0.000 description 1
- 239000003129 oil well Substances 0.000 description 1
- 238000007670 refining Methods 0.000 description 1
- 238000007778 shielded metal arc welding Methods 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/001—Ferrous alloys, e.g. steel alloys containing N
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/44—Ferrous alloys, e.g. steel alloys containing chromium with nickel with molybdenum or tungsten
Definitions
- This invention relates to a method of making a high strength duplex stainless steel and a product of this alloy in either cast or wrought form.
- the material of this invention displays superior toughness, weldability and cracking resistance in H2S bearing environments compared to other duplex stainless steels of similar strength level.
- duplex stainless steels of the prior art have had a number of drawbacks.
- Cast grades generally exhibited only moderate impact toughness at room temperature, and suffered marked losses in toughness as temperatures decreased.
- Duplex grades were also susceptible to serious embrittlement in the heat affected zones (HAZs) of welds. They also exhibited poor resistance to cracking in the sour (H2S-bearing) environments often encountered in oil industry applications. These deficiencies have been major factors inhibiting even wider application of these materials.
- duplex stainless steels are designed to have a microstructure consisting of about 50% ferrite and 50% austenite. It is this microstructure which is responsible for the high strength and good corrosion resistance of these materials.
- the desired ferrite:austenite ratio was obtained only by controlling the composition. This prevented alloy designers from using other techniques for improving the toughness of the ferrite phase which would lead to improved toughness of the total alloy.
- the current invention involves the realization that the ferrite-austenite ratio can be adjusted not only by varying the composition, but also by varying the solution treatment temperature.
- a duplex stainless steel having the following composition Carbon 0.001 to 0.08 Wt. % Manganese 0.001 to 2.00 Wt. % Silicon 0.001 to 1.50 Wt. % Chromium 20.00 to 27.50 Wt. % Nickel 8.00 to 11.00 Wt. % Molybdenum 3.00 to 4.50 Wt. % Sulfur 0.0001 to 0.050 Wt. % Phosphorus 0.0001 to 0.050 Wt. % Nitrogen 0.10 to 0.30 Wt. % Iron Balance is produced.
- composition is balanced such that: where: Creq ⁇ 1.5(%Cr+%Si+%Mo) Nieq ⁇ %Ni+0.3(%Mn)+%Cu+22(%C)+5%N Products of this material are then solution treated by heating to a temperature in the range of 1107°C-1274°C (2050°F-2350°F) and then cooling rapidly as with a water quench.
- the desired yield strength is developed by solution treating at a temperature selected according to the following approximate relationship: Where:
- Patent No. 4,032,367 overlap those of the inventive alloy. Certain compositions of this material combined with certain solution treatment temperatures probably would give a good combination of strength and toughness. However, Patent 4,032,367 does not recognize the relationships between Creq: Nieq ratio, solution treatment temperature and mechanical properties necessary to accomplish this. Obtaining a good combination of strength and toughness with the information given in Patent 4,032,367 would simply be a matter of chance.
- Other patents such as 4,500,351 and 4,055,448 disclose preferred Creq:Nieq relationships, but they differ from those of this invention and are not directly tied to mechanical properties or heat treatment.
- the inventive material Compared to high strength duplex stainless steels of the prior art, the inventive material exhibits considerably greater impact toughness values, particularly at low temperatures. It also exhibits considerably greater impact toughness values in the HAZs of welds. Furthermore, the inventive material exhibits improved resistance to cracking when tested in a simulated sour gas environment according to NACE (National Association of Corrosion Engineers) Test Method TM-01-77.
- NACE National Association of Corrosion Engineers
- This invention is based on the realization that the ferrite contents (strength levels) of high strength duplex stainless steels can be effectively varied not only by adjusting composition, but also by selective use of solution treatment temperature.
- higher solution treatment temperatures than those which have been commonly used for high strength duplex stainless steels, it is possible to obtain the desired ferrite contents (strength levels) using alloy compositions with higher nickel contents for a given content of Cr+Mo+Si. This results in higher nickel contents in the ferrite. Consequently, improvements in low temperature toughness, the toughness of HAZs and resistance to sulfide stress cracking are realized.
- a heat of duplex stainless steel is produced to the following composition: Carbon 0.001 to 0.08 Wt. % Manganese 0.001 to 2.00 Wt. % Silicon 0.001 to 1.50 Wt. % Chromium 20.00 to 27.50 Wt. % Nickel 8.00 to 11.00 Wt. % Molybdenum 3.00 to 4.50 Wt. % Sulfur 0.0001 to 0.050 Wt. % Phosphorus 0.0001 to 0.050 Wt. % Nitrogen 0.10 to 0.30 Wt. % Iron Balance The composition is balanced such that: where: Creq ⁇ 1.5(%Cr+%Si+%Mo) Nieq ⁇ %Ni+0.3(%Mn)+%Cu+22(%C)+5%N
- a product of this material (cast or wrought) is then solution treated by heating to a temperature in the range of 1107°C-1274°C (2050°F-2350°F), followed by rapid cooling (as with a water quench) to prevent formation of deleterious precipitates in the microstructure.
- the specific composition and solution treatment temperature is selected so as to provide the desired combination of yield strength, impact toughness and corrosion resistance.
- FIG. 2 shows a computer-drawn representation of the relationship between chromium equivalent: Nickel equivalent ratio, test temperature and impact toughness for cast material given a 1190°C (2200°F) solution treatment.
- the experimental data used to develop this diagram are presented in Table II. Inspection of the diagram clearly shows that by maintaining low Creq:Nieq ratios, higher impact toughnesses can be realized.
- the superior impact toughness of cast material of the inventive alloy can be appreciated when it is compared to the toughness of other cast duplex stainless steels having similar strength. Two such materials are Alloy 2205 and Ferralium Alloy 255*.
- the impact toughness of these alloys and the inventive alloy are compared in Fig.3. It can be easily seen that the inventive alloy possesses considerably greater impact toughness, particularly at low temperatures. At -87.5°C (-100°F) the lowest impact toughness value of the inventive alloy was about 121.5J (90 ft. lbs)**. The best value of the other two alloys at -87.5°C (-100°F) was below 54J (40 ft. lbs).
- the inventive alloy also shows superior weldability. While high strength duplex stainless steels of the prior art are known to suffer severe embrittlement in the HAZs of welds, this invention produces material which is far more resistant to the problem. In order to illustrate this, test welds were made in cast material from four heats of the inventive alloy, four heats of Ferralium Alloy 255 and one heat of Alloy 2205. Prior to welding, the inventive alloy material had been solution treated at 1190°C (2200°F), while the other materials had been solution treated at 1107°C (2050°F).
- the HAZ impact toughness results are presented in graphical form in Fig.4. While the inventive material did show some loss of toughness (see Table II), the HAZs of the other alloys were seriously degraded in toughness.
- the inventive alloy had HAZ impact toughness values above 67.5J (50 ft. lbs) at -87.5°C (-100°F) while the other two alloys gave values less than 27J (20 ft.lbs) at the same temperatures.
- the corrosion resistance of the inventive alloy is similar to that of high strength duplex stainless steels of the prior art. For chloride-containing environments, this has been established electrochemically. Specimens of the inventive alloy and other duplex stainless steels have been subjected to rapid scan potentio-dynamic tests in a deaerated solution of water plus 5% sodium chloride plus 0.01M hydrochloric acid. The results of this comparison testing are presented in graph form in FIG. 5. Clearly, the test results of the inventive alloy are at least as good as those of any of the other alloys examined. It is appreciated that electrochemical corrosion resistance data are highly dependent upon technique and the specific test method. However, the tests performed were consistent so as to obtain data that were as comparable as possible.
- the material of this invention has superior resistance to cracking in sour (H2S-bearing) environments.
- H2S-bearing sour
- NACE Standard TM-01-77 This test involves stressing tensile specimens of the material being studied in a solution simulating conditions in sour oil wells.
- the solution consists of water, sodium chloride and acetic acid through which hydrogen sulfide and carbon dioxide gases are bubbled.
- Specimens are stressed to various percentages of their yield strengths in order to determine the highest stress level at which fracture does not occur. The higher this stress level, the better the material's cracking resistance.
- compositions can be utilized. These are shown in Table IV. For example, when superior corrosion resistance in chloride-containing environments is desired, composition "C” is advantageously employed. If maximum toughness is desired, composition “A” is preferred. Composition “A” is also preferred for thick-section parts since it is more resistant to formation of deleterious precipitates. Composition “B” offers a combination of improved corrosion resistance compared to Composition “A”, but with improved toughness with respect to Composition “C”. For further clarification, consider the following examples:
- composition "A" would be selected.
- a heat of the inventive alloy would be produced and solution treated at a temperature selected to give the desired yield strength level.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Articles (AREA)
Description
- This invention relates to a method of making a high strength duplex stainless steel and a product of this alloy in either cast or wrought form. The material of this invention displays superior toughness, weldability and cracking resistance in H₂S bearing environments compared to other duplex stainless steels of similar strength level.
- In recent years, a considerable number of high strength austenitic/ferritic duplex stainless steels have been introduced, and the range of applications for these materials has expanded rapidly. The primary reason for this is that these alloys, as a class, offer an attractive combination of strength and corrosion resistance. Typically, these alloys exhibit yield strengths which are about twice those of "ordinary" stainless steels (when compared in the solution treated condition). In terms of general corrosion resistance, these alloys perform quite well in a wide variety of environments. They also have good resistance to localized corrosion and stress corrosion cracking in the presence of chlorides. In resisting these forms of corrosion, the performance of duplex stainless steels often rivals that of far more expensive, more highly-alloyed materials.
- The high strength duplex stainless steels of the prior art, however, have had a number of drawbacks. Cast grades generally exhibited only moderate impact toughness at room temperature, and suffered marked losses in toughness as temperatures decreased. Duplex grades were also susceptible to serious embrittlement in the heat affected zones (HAZs) of welds. They also exhibited poor resistance to cracking in the sour (H₂S-bearing) environments often encountered in oil industry applications. These deficiencies have been major factors inhibiting even wider application of these materials.
- Most high strength duplex stainless steels are designed to have a microstructure consisting of about 50% ferrite and 50% austenite. It is this microstructure which is responsible for the high strength and good corrosion resistance of these materials. In the duplex stainless steels of the prior art, the desired ferrite:austenite ratio was obtained only by controlling the composition. This prevented alloy designers from using other techniques for improving the toughness of the ferrite phase which would lead to improved toughness of the total alloy.
- The current invention involves the realization that the ferrite-austenite ratio can be adjusted not only by varying the composition, but also by varying the solution treatment temperature.
- By using this concept, it is possible to produce a high strength duplex stainless steel having excellent mechanical properties in both cast and wrought forms.
- According to the invention a duplex stainless steel having the following composition
Carbon 0.001 to 0.08 Wt. % Manganese 0.001 to 2.00 Wt. % Silicon 0.001 to 1.50 Wt. % Chromium 20.00 to 27.50 Wt. % Nickel 8.00 to 11.00 Wt. % Molybdenum 3.00 to 4.50 Wt. % Sulfur 0.0001 to 0.050 Wt. % Phosphorus 0.0001 to 0.050 Wt. % Nitrogen 0.10 to 0.30 Wt. % Iron Balance 
where:


Products of this material are then solution treated by heating to a temperature in the range of 1107°C-1274°C (2050°F-2350°F) and then cooling rapidly as with a water quench. For cast products, the desired yield strength is developed by solution treating at a temperature selected according to the following approximate relationship:
Where: - Sy =
- yield strength (0.2% offset) in KSI
- Cr =
-

- Ni =
-

- It should be noted that the composition ranges of Patent No. 4,032,367 overlap those of the inventive alloy. Certain compositions of this material combined with certain solution treatment temperatures probably would give a good combination of strength and toughness. However, Patent 4,032,367 does not recognize the relationships between Creq: Nieq ratio, solution treatment temperature and mechanical properties necessary to accomplish this. Obtaining a good combination of strength and toughness with the information given in Patent 4,032,367 would simply be a matter of chance. Other patents such as 4,500,351 and 4,055,448 disclose preferred Creq:Nieq relationships, but they differ from those of this invention and are not directly tied to mechanical properties or heat treatment.
- Compared to high strength duplex stainless steels of the prior art, the inventive material exhibits considerably greater impact toughness values, particularly at low temperatures. It also exhibits considerably greater impact toughness values in the HAZs of welds. Furthermore, the inventive material exhibits improved resistance to cracking when tested in a simulated sour gas environment according to NACE (National Association of Corrosion Engineers) Test Method TM-01-77.
- The invention will now be further described by way of example with reference to the accompanying drawings, in which:
- Fig.1 is a graph of the empirically derived relationship between composition, solution treatment and temperature and yield strength;
- Fig.2 is a graph of the relationship between Creq:Nieq ratio, test temperature and impact toughness;
- Fig.3 includes three graphs of the impact toughness of inventive alloy and other high strength duplex stainless steels;
- Fig.4 includes three graphs showing HAZ impact toughness of the inventive alloy and other high strength duplex stainless steels; and
- Fig.5 includes four graphs of the pitting resistance of inventive alloy and other high strength duplex stainless steels in de-aerated 5% NaCl+0.01M HCl.
- The invention will also be further described by way of example with reference to the Tables at the end of this description, in which:
- Table 1 is a tabulation of the effects of composition and solution treatment temperature on yield strength;
- Table II is a tabulation of the relationship between Creq:Nieq ratio and impact toughness;
- Table III is a tabulation of the mechanical properties of the inventive alloy; and
- Table IV is a tabulation of the preferred composition ranges of the inventive alloy.
- In cast high strength duplex stainless steels, mechanical property behaviour, microstructure and composition are related in the following manner:
- (1) Strength is primarily related to ferrite content. Higher ferrite contents lead to higher strength levels and lower ferrite contents lead to lower strength levels.
- (2) In material which has been given an appropriate solution treatment, toughness (as reflected by transition temperature) is primarily controlled by the percentage of ferrite, its distribution and its inherent toughness.
- (3) The ferrite content is controlled by the composition of the alloy and by the solution treatment temperature.
- (4) The composition of the ferrite is controlled by the composition of the alloy and by the solution treatment temperature.
- (5) The inherent toughness of ferrite is controlled by its composition. As with ferritic stainless steels, increasing the nickel content of the ferrite phase increases its inherent toughness.
- In the prior art, it has been the practice to solution treat high strength duplex stainless steels at temperatures similar to those used for "ordinary" austenitic stainless steels (e.g. 1083°C-1107°C i.e. 2000°F to 2050°F). The desired strength levels have been obtained simply by adjusting the composition to achieve the necessary ferrite content. Because of this practice, it has been necessary to maintain relatively high ratios of ferrite forming elements (Cr, Si and Mo) to austenite forming elements (Ni, Cu, C and N). Consequently, the nickel levels of available high strength duplex stainless steels have been relatively low, generally in the range of 4% to 7%. This, in turn, has resulted in low nickel contents in the ferrite and ultimately in poor low temperature toughness in these materials.
- This invention is based on the realization that the ferrite contents (strength levels) of high strength duplex stainless steels can be effectively varied not only by adjusting composition, but also by selective use of solution treatment temperature. By employing higher solution treatment temperatures than those which have been commonly used for high strength duplex stainless steels, it is possible to obtain the desired ferrite contents (strength levels) using alloy compositions with higher nickel contents for a given content of Cr+Mo+Si. This results in higher nickel contents in the ferrite. Consequently, improvements in low temperature toughness, the toughness of HAZs and resistance to sulfide stress cracking are realized.
- In the practice of this invention, a heat of duplex stainless steel is produced to the following composition:
Carbon 0.001 to 0.08 Wt. % Manganese 0.001 to 2.00 Wt. % Silicon 0.001 to 1.50 Wt. % Chromium 20.00 to 27.50 Wt. % Nickel 8.00 to 11.00 Wt. % Molybdenum 3.00 to 4.50 Wt. % Sulfur 0.0001 to 0.050 Wt. % Phosphorus 0.0001 to 0.050 Wt. % Nitrogen 0.10 to 0.30 Wt. % Iron Balance
The composition is balanced such that:
where:


- A product of this material (cast or wrought) is then solution treated by heating to a temperature in the range of 1107°C-1274°C (2050°F-2350°F), followed by rapid cooling (as with a water quench) to prevent formation of deleterious precipitates in the microstructure. For cast products, the specific composition and solution treatment temperature is selected so as to provide the desired combination of yield strength, impact toughness and corrosion resistance.
- For cast material having a composition covered by this patent, it has been determined empirically that yield strength, composition and solution treatment temperature are related by the following approximate relationship:
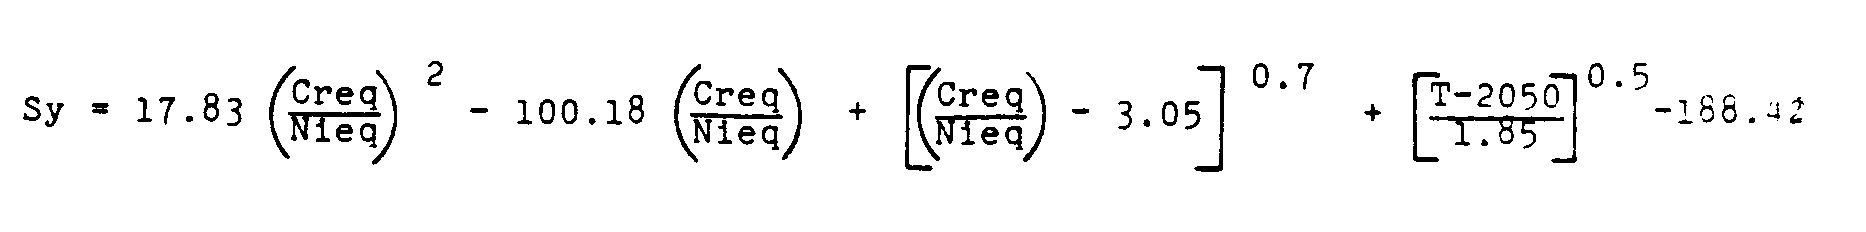
Where: - Sy =
- yield strength (0.2% offset) in KSI (1 KSI = 6.895 MPa)
- Cr =
-

- Ni =
-
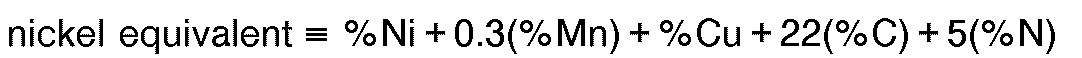
- The relationship described above makes use of a ratio of ferrite forming elements (chromium equivalent) to austenite forming elements (nickel equivalent). It has been found that this ratio can also be used to insure that good impact toughness is maintained.
- FIG. 2 shows a computer-drawn representation of the relationship between chromium equivalent: Nickel equivalent ratio, test temperature and impact toughness for cast material given a 1190°C (2200°F) solution treatment. The experimental data used to develop this diagram are presented in Table II. Inspection of the diagram clearly shows that by maintaining low Creq:Nieq ratios, higher impact toughnesses can be realized.
- The rationale for choosing the upper and lower Creq:Nieq ratio limits (3.50 and 4.00 respectively) can be understood by examining FIGS. 1 and 2. The lower limit was set at 3.50 since this appears to be the lowest value at which a yield strength of 65KSI can be guaranteed in cast material given the range of solution treatment temperatures covered in this patent. For many applications where a duplex stainless steel such as this would be used, a minimum yield strength of 448.2 MPa (65 KSI) is required. The upper limit was set at 4.00 since beyond this level, impact toughness values deteriorate markedly. Although the Creq and Nieq expressions of this patent were not specifically devised to describe other high strength duplex stainless steels, it should be pointed out that they are typically produced with much higher Creq:Nieq ratios than the inventive alloy. This would tend to place them in the lower toughness regions of the diagram in FIG. 2.
- Mechanical properties of cast material from five heats of the inventive alloy are shown in Table III. Also shown are mechanical properties from one heat of forged material. The compositions of these heats may be found in Table I and in all cases, the solution treatment temperature was 1190°C (2200°F). All five heats of the cast material as well as the wrought material show an excellent combination of strength and toughness. All testing was performed according to ASTM A 370-77.
- The superior impact toughness of cast material of the inventive alloy can be appreciated when it is compared to the toughness of other cast duplex stainless steels having similar strength. Two such materials are
Alloy 2205 andFerralium Alloy 255*. The impact toughness of these alloys and the inventive alloy are compared in Fig.3. It can be easily seen that the inventive alloy possesses considerably greater impact toughness, particularly at low temperatures. At -87.5°C (-100°F) the lowest impact toughness value of the inventive alloy was about 121.5J (90 ft. lbs)**. The best value of the other two alloys at -87.5°C (-100°F) was below 54J (40 ft. lbs). A level of about 101.25J (75 ft.lbs) is distinctly advantageous over high strength duplex stainless steels of the prior art. All of these data were obtained using standard charpy specimens taken from cast keel bars. The inventive alloy material was solution treated at 1190°C (2200°F) while the other alloys were solution treated at their recommended temperature 1107°C (2050°F). All tests were performed in accordance with ASTM A370-77.
* Registered Trademark of Bonar-Langley Alloys Ltd., United Kingdom.
** 1 ft. lb = 1.35J. - It should be pointed out that all of the impact toughness data presented for the inventive alloy were obtained from air-melt induction heats. Other melting processes which result in greater cleanliness (i.e. AOD or VOD refining) can be expected to result in even greater toughness values. For example, two recent AOD-refined heats of the inventive alloy had impact toughness values approximately 25% higher than air-melt induction heats of similar Creq:Nieq ratio.
- The inventive alloy also shows superior weldability. While high strength duplex stainless steels of the prior art are known to suffer severe embrittlement in the HAZs of welds, this invention produces material which is far more resistant to the problem. In order to illustrate this, test welds were made in cast material from four heats of the inventive alloy, four heats of
Ferralium Alloy 255 and one heat ofAlloy 2205. Prior to welding, the inventive alloy material had been solution treated at 1190°C (2200°F), while the other materials had been solution treated at 1107°C (2050°F). The welding procedure employed was as follows:
Process - SMAW
Filler Material - Sandvik 22.9.3 (4mm Dia.)
Preheat - None
Current - 135 AMPS
Polarity - DCRP
Interpass Temp - 79°C (200°F) Max
Post Weld Heat Treatment - None - After welding, standard charpy impact specimens were removed from the welded plates such that the specimen notches were located in the HAZs of the welds. The specimens were then tested according to ASTM A370-77.
- The HAZ impact toughness results are presented in graphical form in Fig.4. While the inventive material did show some loss of toughness (see Table II), the HAZs of the other alloys were seriously degraded in toughness. The inventive alloy had HAZ impact toughness values above 67.5J (50 ft. lbs) at -87.5°C (-100°F) while the other two alloys gave values less than 27J (20 ft.lbs) at the same temperatures.
- In many environments, the corrosion resistance of the inventive alloy is similar to that of high strength duplex stainless steels of the prior art. For chloride-containing environments, this has been established electrochemically. Specimens of the inventive alloy and other duplex stainless steels have been subjected to rapid scan potentio-dynamic tests in a deaerated solution of water plus 5% sodium chloride plus 0.01M hydrochloric acid. The results of this comparison testing are presented in graph form in FIG. 5. Clearly, the test results of the inventive alloy are at least as good as those of any of the other alloys examined. It is appreciated that electrochemical corrosion resistance data are highly dependent upon technique and the specific test method. However, the tests performed were consistent so as to obtain data that were as comparable as possible.
- Compared to other cast high strength duplex stainless steels, the material of this invention has superior resistance to cracking in sour (H₂S-bearing) environments. In evaluating materials for service in sour environments, it is common to employ tests conducted according to NACE Standard TM-01-77. This test involves stressing tensile specimens of the material being studied in a solution simulating conditions in sour oil wells. The solution consists of water, sodium chloride and acetic acid through which hydrogen sulfide and carbon dioxide gases are bubbled. Specimens are stressed to various percentages of their yield strengths in order to determine the highest stress level at which fracture does not occur. The higher this stress level, the better the material's cracking resistance.
- Specimens from three heats of the inventive alloy (71545, 72497 and 72847) have been tested. These have survived 720 hours (the duration of the standard test) unbroken at stress levels up to and including 80% of their yield strengths. In addition, specimens containing welds in their gage lengths (both as welded and resolution treated) have passed the test at 80% of the base metal's yield strength. As far as is known, no other cast duplex stainless steels of similar strength level have been able to perform this well.
- Depending upon the characteristics desired, certain narrower preferred ranges of alloying elements can be utilized. These are shown in Table IV. For example, when superior corrosion resistance in chloride-containing environments is desired, composition"C" is advantageously employed. If maximum toughness is desired, composition "A" is preferred. Composition "A" is also preferred for thick-section parts since it is more resistant to formation of deleterious precipitates. Composition "B" offers a combination of improved corrosion resistance compared to Composition "A", but with improved toughness with respect to Composition "C". For further clarification, consider the following examples:
- Suppose it was desired to produce a small valve body having good-to-excellent corrosion resistance in the presence of chlorides, a minimum yield strength of 448.2 MPa (65 KSI) and a minimum impact toughness of 101.25J (75 ft/lbs) at -87.5°C (-100°F). Since the size of the casting is small and the degree of corrosion resistance must be high, composition "C" would be selected. A heat of the inventive alloy would be produced having a composition falling within the limits of "C". An example of such a heat is Heat 72497, which had the following actual composition:
C 0.039% Mn 0.54 Si 1.05 Cr 24.59 Ni 9.83 Mo 3.51 Cu 0.11 N 0.198 Fe Balance - Suppose it was desired to produce a large pump casting requiring excellent toughness in relatively heavy sections. A yield strength of 70 KSI minimum and moderate corrosion resistance in the presence of chlorides. Since thick sections are involved and extreme corrosion resistance is not required, composition "A" would be selected. As in the previous example, a heat of the inventive alloy would be produced and solution treated at a temperature selected to give the desired yield strength level.
- Experimental Heat 70335 had a composition which would be acceptable for this application:
C 0.052% Mn 0.44 Si 1.20 Cr 20.88 Ni 9.05 Mo 3.83 Cu 0.18 N 0.13 Fe Balance
For this composition, Fig.2 indicates that a solution treatment temperature of 1190°C (2200°F) should be adequate to obtain a yield strength level of 482.65 MPa (70 KSI). When material from Heat 70335 was solution treated at 1190°C (2200°F), the resulting yield strength was 70.5 KSI. The impact toughness at -87.5°C (-100°F) averaged 186.3J (138 ft-lbs). As in the previous example, these properties would meet the required values.


Claims (6)
- A duplex stainless steel having austenite pools in a ferrite matrix resulting from heating to a temperature in the range of 1107°C-1274°C (2050°F-2350°F) and cooling rapidly thereafter, said steel consisting
Carbon 0.001 to 0.08 Wt. % Manganese 0.001 to 2.00 Wt. % Silicon 0.001 to 1.50 Wt. % Chromium 20.00 to 27.50 Wt. % Nickel 8.00 to 11.00 Wt. % Molybdenum 3.00 to 4.50 Wt. % Sulfur 0.0001 to 0.050 Wt. % Phosphorus 0.0001 to 0.050 Wt. % Nitrogen 0.10 to 0.30 Wt. % Iron Balance 


and having greater impact toughness values in the cast form than Ferralium Alloy 255 and SAF 2205, the impact toughness in Charpy V-notch testing at -87.5°C (-100°F) being above 101.25J (75 ft. lbs) when tested from keel blocks per ASTM E23-82, the HAZ impact toughness at -87.5°C (-100°F) being above about 67.5J (50 ft.lbs) and having a yield st rength of at least 448.2 MPa (65 KSI). - A duplex stainless steel according to claim 1, characterized by comprising:
Wt.% Carbon 0.07 MAX Manganese 2.00 MAX Silicon 1.50 MAX Chromium 20.50 - 22.50 Nickel 8.00 - 9.50 Molybdenum 3.00 - 4.00 Nitrogen 0.10 - 0.25 Sulfur 0.025 MAX Phosphorus 0.04 MAX. - A duplex stainless steel according to claim 1, characterized by comprising:
wt.% Carbon 0.07 MAX Manganese 2.00 MAX Silicon 1.50 MAX Chromium 22.50 - 24.00 Nickel 8.50 - 10.00 Molybdenum 3.00 - 4.00 Nitrogen 0.15 - 0.25 Sulfur 0.025 MAX Phosphorus 0.04 MAX - A duplex stainless steel according to claim 1, characterized by comprising:
wt.% Carbon 0.07 MAX Manganese 2.00 MAX Silicon 1.50 MAX Chromium 23.50 - 26.00 Nickel 9.00 - 10.50 Molybdenum 3.00 - 4.00 Nitrogen 0.15 - 0.25 Sulfur 0.025 MAX Phosphorus 0.04 MAX - A method of producing a duplex stainless steel characterized by producing a heat of duplex stainless steel having a composition as set out in any one of claims 1 to 4, and solution treating by heating to a temperature in the range of from 1107°C-1274°C (2050°F-2350°F).
- A method as claimed in claim 5, characterized by rapid cooling after the solution treatment.
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US06/864,333 US4715908A (en) | 1985-11-26 | 1986-05-19 | Duplex stainless steel product with improved mechanical properties |
| DE19873781160 DE3781160T2 (en) | 1987-12-17 | 1987-12-17 | METHOD FOR PRODUCING STAINLESS DUPLEX STEEL AND COMPONENTS FROM STAINLESS STEEL DUPLEX STEEL WITH IMPROVED MECHANICAL PROPERTIES. |
| EP19870311114 EP0320548B1 (en) | 1987-12-17 | 1987-12-17 | Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP19870311114 EP0320548B1 (en) | 1987-12-17 | 1987-12-17 | Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0320548A1 EP0320548A1 (en) | 1989-06-21 |
| EP0320548B1 true EP0320548B1 (en) | 1992-08-12 |
Family
ID=8198148
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19870311114 Expired EP0320548B1 (en) | 1985-11-26 | 1987-12-17 | Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0320548B1 (en) |
| DE (1) | DE3781160T2 (en) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AT397515B (en) * | 1990-05-03 | 1994-04-25 | Boehler Edelstahl | HIGH-STRENGTH CORROSION-RESISTANT DUPLEX ALLOY |
| US5411545A (en) * | 1994-03-14 | 1995-05-02 | Medtronic, Inc. | Medical electrical lead |
| CN114346142B (en) * | 2022-01-18 | 2023-07-14 | 山西太钢不锈钢股份有限公司 | A forging method for improving low-temperature impact toughness of S32750 super duplex stainless steel round steel |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1307401A (en) * | 1970-03-18 | 1973-02-21 | Nippon Kokan Kk | Austenitic heat resisting stainless steel |
| US4405389A (en) * | 1982-10-21 | 1983-09-20 | Ingersoll-Rand Company | Austenitic stainless steel casting alloy for corrosive applications |
| US4500351A (en) * | 1984-02-27 | 1985-02-19 | Amax Inc. | Cast duplex stainless steel |
| SE453838B (en) * | 1985-09-05 | 1988-03-07 | Santrade Ltd | HIGH-QUALITY FERRIT-AUSTENITIC STAINLESS STEEL |
-
1987
- 1987-12-17 DE DE19873781160 patent/DE3781160T2/en not_active Expired - Fee Related
- 1987-12-17 EP EP19870311114 patent/EP0320548B1/en not_active Expired
Also Published As
| Publication number | Publication date |
|---|---|
| EP0320548A1 (en) | 1989-06-21 |
| DE3781160D1 (en) | 1992-09-17 |
| DE3781160T2 (en) | 1993-03-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2165817C (en) | Ferritic-austenitic stainless steel and use of the steel | |
| US6749697B2 (en) | Duplex stainless steel | |
| EP2358918B1 (en) | Ferritic-austenitic stainless steel | |
| US5407635A (en) | Low-chromium ferritic heat-resistant steel with improved toughness and creep strength | |
| AU2002328002B2 (en) | Duplex steel alloy | |
| Wang et al. | Nickel-free duplex stainless steels | |
| US6322642B1 (en) | Process and steel for the manufacture of a pressure vessel working in the presence hydrogen sulfide | |
| JPS61130462A (en) | High-touchness extra high tension steel having superior stress corrosion cracking resistance as well as yield stress of 110kgf/mm2 and above | |
| US20030133823A1 (en) | Use of a duplex stainless steel alloy | |
| KR20090078813A (en) | Duplex Stainless Steel Alloys and Their Uses | |
| US20070089810A1 (en) | Duplex stainless steel alloy for use in seawater applications | |
| US20100084121A1 (en) | Plate | |
| EP0411515A1 (en) | High strength heat-resistant low alloy steels | |
| JPH05287455A (en) | Martensitic stainless steel for oil well | |
| EP3960881A1 (en) | Austenitic stainless steel | |
| EP0438992B1 (en) | Austenitic stainless steel | |
| AU2002242314A2 (en) | Duplex stainless steels | |
| US9669482B2 (en) | Submarine hull steel having enhanced weldability | |
| US4715908A (en) | Duplex stainless steel product with improved mechanical properties | |
| US6136109A (en) | Method of manufacturing high chromium martensite steel pipe having excellent pitting resistance | |
| EP0320548A1 (en) | Method of making a duplex stainless steel and a duplex stainless steel product with improved mechanical properties | |
| JPH07290275A (en) | Welding wire for high strength Cr-Mo steel | |
| JPH06930B2 (en) | Manufacturing method of extra-thick, low-weldability high-strength steel with excellent resistance to hydrogen sulfide stress corrosion cracking and low temperature toughness | |
| CA1299071C (en) | Method of making a duplex stainless steel and duplex stainless steel product with improved mechanical properties | |
| JPH08134593A (en) | High-strength austenitic alloy with excellent resistance to seawater corrosion and hydrogen sulfide corrosion |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB SE |
|
| 17P | Request for examination filed |
Effective date: 19890731 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: ESCO CORPORATION |
|
| 17Q | First examination report despatched |
Effective date: 19910325 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB SE |
|
| REF | Corresponds to: |
Ref document number: 3781160 Country of ref document: DE Date of ref document: 19920917 |
|
| ET | Fr: translation filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19921208 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19921229 Year of fee payment: 6 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26N | No opposition filed | ||
| 26 | Opposition filed |
Opponent name: SANDVIK AKTIEBOLAG Effective date: 19930512 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: SANDVIK AKTIEBOLAG PATENT DEPARTMENT Effective date: 19930512 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19931108 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19931119 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19940831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19940901 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 87311114.0 |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| 27W | Patent revoked |
Effective date: 19941219 |
|
| GBPR | Gb: patent revoked under art. 102 of the ep convention designating the uk as contracting state |
Free format text: 941219 |