EP0178310B1 - Pneumatic charger for feeding pulverized and granular materials into metal melts - Google Patents
Pneumatic charger for feeding pulverized and granular materials into metal melts Download PDFInfo
- Publication number
- EP0178310B1 EP0178310B1 EP19850901541 EP85901541A EP0178310B1 EP 0178310 B1 EP0178310 B1 EP 0178310B1 EP 19850901541 EP19850901541 EP 19850901541 EP 85901541 A EP85901541 A EP 85901541A EP 0178310 B1 EP0178310 B1 EP 0178310B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- charger
- gas
- insert
- box
- wind
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
Images
Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F27—FURNACES; KILNS; OVENS; RETORTS
- F27D—DETAILS OR ACCESSORIES OF FURNACES, KILNS, OVENS OR RETORTS, IN SO FAR AS THEY ARE OF KINDS OCCURRING IN MORE THAN ONE KIND OF FURNACE
- F27D3/00—Charging; Discharging; Manipulation of charge
- F27D3/16—Introducing a fluid jet or current into the charge
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21C—PROCESSING OF PIG-IRON, e.g. REFINING, MANUFACTURE OF WROUGHT-IRON OR STEEL; TREATMENT IN MOLTEN STATE OF FERROUS ALLOYS
- C21C7/00—Treating molten ferrous alloys, e.g. steel, not covered by groups C21C1/00 - C21C5/00
- C21C7/0037—Treating molten ferrous alloys, e.g. steel, not covered by groups C21C1/00 - C21C5/00 by injecting powdered material
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B9/00—General processes of refining or remelting of metals; Apparatus for electroslag or arc remelting of metals
- C22B9/10—General processes of refining or remelting of metals; Apparatus for electroslag or arc remelting of metals with refining or fluxing agents; Use of materials therefor, e.g. slagging or scorifying agents
- C22B9/103—Methods of introduction of solid or liquid refining or fluxing agents
Definitions
- the invention relates to a pneumatic charger for the transport of granular or pulverized inflammable and explosive materials as well as materials of high density into metal melts.
- Metallurgical processes used in metallurgy show a new tread of development. A considerable part of the processes have been relocated from the metallurgic furnace into the ladle.
- One of the most important branches of the ladle-metallurgic processes thus developed is represented by the blowing technologies, in course of which the gas carrying the diverse materials is blown, resp. transported pneumatically into the metal bath.
- the most known equipment for treating steels is the blower available in sale with the trade-mark "Scandinavian Lancers".
- pulverized treating material having a calcium- silicon content is introduced pneumatically into the steel.
- the main part of the charger is a conical fluidizator, consisting of a dense screeing cloth and the nozzles with a small cross-section arranged behind the screeing cloth, which enables the uniform distribution of the gas.
- the equipment is operated with an indifferent gas, with argon, pressure prevailing in the tank amounts to 6-8 bars.
- the gas gets mixed with the pulverized reagent.
- High pressure presses the mixture of gas and powder into the delivery pipeline and via the lancer into the metal bath.
- Due to wear of the screen and obstruction of the nozzles the fluidizator requires permanent maintenance.
- the powder tends to clogging in the tank, material to be blown cannot be stored for a longer time.
- a further disadvantageous feature of the equipment lies in that it can be operated with high-pressure gas only.
- Another mechanical equipment is also known which is different from that specified above, in so far as its fluidizator is formed by a screening cloth arranged at an angle of 30° and it is provided with a lower discharge opening with variable cross-section.
- Speed of material stream is controlled by a mechanical feeder. In respect to construction this equipment is far more complicated, possibilities of failure are greater. At the same time vibrations of the mechanical feeder make weighing more difficult.
- the aforementioned equipments operate on the principle of fluidization.
- the carrier gas transfers its pulse to the material grains to be transported. If the force resulting from the pulse is higher, than the effect resulting from the weight of the grains and the frictional force arising inbetween, the particles are carried away by the gas, accordingly delivery is performed.
- state of fluidization depends partly on the streaming conditions of the carrying gas, partly on the grainsize and density of the material to be transported. Accordingly, this condition cannot be realized with materials of large grain-size and density-e.g. with ferro-alloys-and if, with considerable difficulties only.
- a device for charging a gas stream with pulverized materials comprising a closed cylindrical material storage tank, being set under pressure and constructed at its lower portion as a conus, which is provided with a screen-like device, enabling the gas suspending the pulverized material.
- the top of the tank, the conus and the end of conus are provided with openings, connected with conduits or pipes communicating with a delivery duct, containing the pressurized transport gas.
- the pressure and the flow through of the gas are controlled by several valves, a pressure gauge and a flow through meter.
- This device needs high pressure to press the mixture of gas and powder into the delivery duct.
- due to the wear of the screen and the obstruction of the nozzle of the conus permanent maintenance is required.
- the aim of the invention is to develop a solution with which parameters of transport, so transport capacity, density of delivery, quantity of carrier gas are constant, while at the same time, in case of necessity these values could be easily changed to the desired extent and in dependence of mode of operation.
- the solution according to the invention is well adapted for the transport of materials with a grain size of 3 to 5 mm and a density of 4 to 6 kg/dm 3 . Construction of the equipment is resistant to increased loads occurring under metallurgical circumstances.
- the invention relates to a pneumatic charger for the transport of pulverized and granular materials into metal melts, comprising a windbox connected to the conical bottom of the material storage tank, a porous element of cylindrical shape being arranged in a vertical position forming a structural unit with said wind-box, an exchangeable insert with a bore, the top of which being positioned in the free room formed by said porous element, and further comprising a tap communicating with the insert and a T-pipe connection.
- the material storage tank 1 receives the material to be transported, being a pressure-proof tank with a conical lower part and provided with an opening for material filling.
- the cone of the tank 1 ends in the flanged connection 2.
- the wind-box 4 is forming a unit with the counter-part of the flange 2. Said wind-box is formed with the sleeve 3 which is clamping the porous element 5 at the top, while the lower part of the element 5 is seated on the bottom of the box 4.
- the box 4 communicates with the inlet stud 6 introducing the gas at a pre-set pressure.
- the mixture of gas and material is flowing through the cylindrical bore of the insert 7.
- the insert 7 with the bore is clamped with a releasable bond 8 and is provided with the sealing 9.
- Material flow is interrupted by the tap 10, while the mixture of gas and material flowing through the tap 10 streams by the aid of the T-pipe connection 11 into the pipeline system.
- Gas in a controlled quantity is introduced into the inlet stud of the T-pipe connection 11, whereas its output branch is connected to the injecting lancer through the delivery duct.
- T-pipe connection 11 does not contain any structural element which would impede material flow, it does not exert a higher flow resistance, than an average pipe tract. In such a manner it becomes possible to connect the feeders of two or more material storage tanks in series.
- the pneumatic charger according to the invention operates, as follows:
- Material storage tank 1 is filled with the material to be blown, now the tap 10 is closed. After having closed the filling opening, gas at a pre-set pressure is led to the tank 1 through the inlet stud 6.
- gas at a pre-set pressure is led to the tank 1 through the inlet stud 6.
- First one starts with the diving of the lancer into the metal bath and simultaneously gas in a controlled quantity is introduced into the inlet stud of the T-pipe connection 11, the pressure of which prevents penetration of metal into the inside of the lancer.
- material feeding begins by opening the tap 10.
- gas is streaming among the material grains, through the porous element 5 to the insert 7. Material grains to be found on the upper bevelled part of the insert 7 are carried away by the streaming gas.
- the gas-material mixture is considerably accelerated in the bore of the insert and arrives with a significant kinetic energy to the T-pipe connection 11. Taking into consideration that in respect to the proportion gas/solids this mixture is very dense, controlled gas quantity, as previously mentioned, is admixed here. In such a manner it can be achieved that the material arrives pneumatically from the storage tank to the metal bath through the delivery duct and the lancer.
- the porous element 5 is a cylinder with a vertical axis, so powder fraction of the material to be delivered cannot deposit in the opening thereof, so required cleaning and maintenance are minimal.
- Delivery output is uniform, at the same time it can be easily controlled in dependence of mode of operation, magnitude depends on the flow velocity having been developed in the bore of the insert 7. Control can be easily performed without changing any structural element, simply by regulating the pressure of gas streaming through the stud 6.
- the charger according to the invention yield several new possibilities in the field of blowing technology.
- a plurality of metallurgic processes can be performed with the same equipment.
- the tap 10 of one or of the other tank by opening the tap 10 of one or of the other tank, different materials can be introduced one after the other, or by the simultaneous opening of the taps 10 mixing of the materials while blowing becomes also possible.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Furnace Charging Or Discharging (AREA)
- Air Transport Of Granular Materials (AREA)
Abstract
Description
- The invention relates to a pneumatic charger for the transport of granular or pulverized inflammable and explosive materials as well as materials of high density into metal melts.
- Metallurgical processes used in metallurgy show a new tread of development. A considerable part of the processes have been relocated from the metallurgic furnace into the ladle. One of the most important branches of the ladle-metallurgic processes thus developed is represented by the blowing technologies, in course of which the gas carrying the diverse materials is blown, resp. transported pneumatically into the metal bath.
- As a result of the process several material qualities not having been manufactured as mass-produced goods up to now can be produced in a large quantity, or production of tradiational qualities can be rendered more economical. In dependence of metallurgic processes the materials to be blown vary in respect to chemical composition and grain distribution within wide ranges. Accordingly, grain size may vary from a few microns to several millimetres, while chemical composition may vary from the treating materials on calcium basis through ground ferro-alloys to the granular alloys containing magnesium having a thermite character and being inflammable and explosive. In dependence of the quality of treating materials chargers of different structures are in use. In the initial period methods developed from mechanical feeders well proved in pneumatic material delivery to mechanic-pneumatic modes of feeding, arriving at last to chargers based exclusively on the principle of pneumatics.
- The most known equipment for treating steels is the blower available in sale with the trade-mark "Scandinavian Lancers". In course of said technologies pulverized treating material having a calcium- silicon content is introduced pneumatically into the steel. The main part of the charger is a conical fluidizator, consisting of a dense screeing cloth and the nozzles with a small cross-section arranged behind the screeing cloth, which enables the uniform distribution of the gas.
- . The equipment is operated with an indifferent gas, with argon, pressure prevailing in the tank amounts to 6-8 bars. In the fluidizator the gas gets mixed with the pulverized reagent. High pressure presses the mixture of gas and powder into the delivery pipeline and via the lancer into the metal bath. Due to wear of the screen and obstruction of the nozzles the fluidizator requires permanent maintenance. The powder tends to clogging in the tank, material to be blown cannot be stored for a longer time. A further disadvantageous feature of the equipment lies in that it can be operated with high-pressure gas only.
- Another mechanical equipment is also known which is different from that specified above, in so far as its fluidizator is formed by a screening cloth arranged at an angle of 30° and it is provided with a lower discharge opening with variable cross-section. Speed of material stream is controlled by a mechanical feeder. In respect to construction this equipment is far more complicated, possibilities of failure are greater. At the same time vibrations of the mechanical feeder make weighing more difficult.
- The aforementioned equipments operate on the principle of fluidization. When passing through the fluidizing element, the carrier gas transfers its pulse to the material grains to be transported. If the force resulting from the pulse is higher, than the effect resulting from the weight of the grains and the frictional force arising inbetween, the particles are carried away by the gas, accordingly delivery is performed. As a consequence, state of fluidization depends partly on the streaming conditions of the carrying gas, partly on the grainsize and density of the material to be transported. Accordingly, this condition cannot be realized with materials of large grain-size and density-e.g. with ferro-alloys-and if, with considerable difficulties only.
- If-inspite of the arising difficulties-the desired condition can be achieved, streams of high speed occurring in course of fluidization are considerably wearing the fluidizing elements, simultaneously friction arising between the grains to be transported may lead to self-ignition. Hazard of fire and explosion increases with material having magnesium content. With these types inflammability is increased by the small grainsize and arising high speeds, being otherwise most advantageous for the fluidizing process. By these reasons alloys with magnesium content are blown in not frequently.
- Further by the DE-B-1148938 a device for charging a gas stream with pulverized materials is known, comprising a closed cylindrical material storage tank, being set under pressure and constructed at its lower portion as a conus, which is provided with a screen-like device, enabling the gas suspending the pulverized material. The top of the tank, the conus and the end of conus are provided with openings, connected with conduits or pipes communicating with a delivery duct, containing the pressurized transport gas. The pressure and the flow through of the gas are controlled by several valves, a pressure gauge and a flow through meter. This device needs high pressure to press the mixture of gas and powder into the delivery duct. Thus, due to the wear of the screen and the obstruction of the nozzle of the conus permanent maintenance is required.
- The aim of the invention is to develop a solution with which parameters of transport, so transport capacity, density of delivery, quantity of carrier gas are constant, while at the same time, in case of necessity these values could be easily changed to the desired extent and in dependence of mode of operation. The solution according to the invention is well adapted for the transport of materials with a grain size of 3 to 5 mm and a density of 4 to 6 kg/dm3. Construction of the equipment is resistant to increased loads occurring under metallurgical circumstances.
- Accordingly, the invention relates to a pneumatic charger for the transport of pulverized and granular materials into metal melts, comprising a windbox connected to the conical bottom of the material storage tank, a porous element of cylindrical shape being arranged in a vertical position forming a structural unit with said wind-box, an exchangeable insert with a bore, the top of which being positioned in the free room formed by said porous element, and further comprising a tap communicating with the insert and a T-pipe connection.
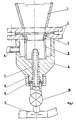
- The invention will now be described in detail by means of a preferred embodiment of the invention, by the aid of the drawing enclosed, illustrating the pneumatic charger in a sectional view.
- The material storage tank 1 receives the material to be transported, being a pressure-proof tank with a conical lower part and provided with an opening for material filling. The cone of the tank 1 ends in the
flanged connection 2. The wind-box 4 is forming a unit with the counter-part of theflange 2. Said wind-box is formed with thesleeve 3 which is clamping theporous element 5 at the top, while the lower part of theelement 5 is seated on the bottom of the box 4. The box 4 communicates with theinlet stud 6 introducing the gas at a pre-set pressure. The mixture of gas and material is flowing through the cylindrical bore of theinsert 7. Theinsert 7 with the bore is clamped with a releasable bond 8 and is provided with the sealing 9. Material flow is interrupted by thetap 10, while the mixture of gas and material flowing through thetap 10 streams by the aid of the T-pipe connection 11 into the pipeline system. Gas in a controlled quantity is introduced into the inlet stud of the T-pipe connection 11, whereas its output branch is connected to the injecting lancer through the delivery duct. - As the T-
pipe connection 11 does not contain any structural element which would impede material flow, it does not exert a higher flow resistance, than an average pipe tract. In such a manner it becomes possible to connect the feeders of two or more material storage tanks in series. - This fact opens new possibilities in respect to blowing technology.
- The pneumatic charger according to the invention operates, as follows:
- Material storage tank 1 is filled with the material to be blown, now the
tap 10 is closed. After having closed the filling opening, gas at a pre-set pressure is led to the tank 1 through theinlet stud 6. First one starts with the diving of the lancer into the metal bath and simultaneously gas in a controlled quantity is introduced into the inlet stud of the T-pipe connection 11, the pressure of which prevents penetration of metal into the inside of the lancer. In the lower position of the lancer, when it is already dipped into the metal bath, material feeding begins by opening thetap 10. Through theinlet stud 6 gas is streaming among the material grains, through theporous element 5 to theinsert 7. Material grains to be found on the upper bevelled part of theinsert 7 are carried away by the streaming gas. The gas-material mixture is considerably accelerated in the bore of the insert and arrives with a significant kinetic energy to the T-pipe connection 11. Taking into consideration that in respect to the proportion gas/solids this mixture is very dense, controlled gas quantity, as previously mentioned, is admixed here. In such a manner it can be achieved that the material arrives pneumatically from the storage tank to the metal bath through the delivery duct and the lancer. - As the material to be transported is forwarded by its own weight to the
insert 7, it is to be considered as specifically advantageous, that feeding is independent of material density and grain size. - Operational safety of the equipment is far increased by the fact that in course of feeding no fluidization flow is taking place, the porous element is neither mechanically nor abrasively loaded. Flows with a higher velocity are transferred to the
insert 7, which can be easily manufactured from a wear-resistant structural material. At the same time theinsert 7 is clamped into the wind-box with a releasable bond 8, enabling an easy and quick exchange. - The
porous element 5 is a cylinder with a vertical axis, so powder fraction of the material to be delivered cannot deposit in the opening thereof, so required cleaning and maintenance are minimal. - Delivery output is uniform, at the same time it can be easily controlled in dependence of mode of operation, magnitude depends on the flow velocity having been developed in the bore of the
insert 7. Control can be easily performed without changing any structural element, simply by regulating the pressure of gas streaming through thestud 6. - In course of the blowing process, up to the full immersion of the lancer, the pressure of the streaming gas on the inlet side of the T-
pipe connection 11 prevents intrusion of metal into the inside of the lancer. The streaming of the material to be blown begins in the lower position of the lancer, i.e. in a completely immersed position, with the opening of thetap 10. In contrast to known equipments, by using the solution according to the invention accidents resulting from considerable squirting-occurring frequently with alloys containing magnesium―can be avoided. This phenomenon can be observed especially, if in course of the immersion of the laser material is blown into low bath denth - The charger according to the invention yield several new possibilities in the field of blowing technology. In case, if the T-
pipe connection 11 of the blowers of two or more material storage tanks are connected in series, a plurality of metallurgic processes can be performed with the same equipment. In the immersed state of the lancer, by opening thetap 10 of one or of the other tank, different materials can be introduced one after the other, or by the simultaneous opening of thetaps 10 mixing of the materials while blowing becomes also possible. - As it becomes obvious from all what has been said, inspite of the simple construction, the equipment performs all the functions required by the special circumstances of blowing technology in course of pneumatic transport.
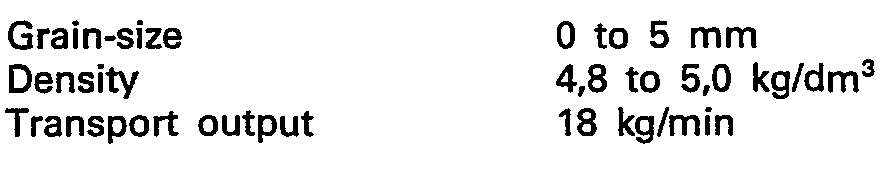
- Some advantageous features of the invention will be demonstrated by the way of examples.
- In course of the experiment calcium containing mineral material and-without lifting the lancer- magnesium containing auxiliary alloy were introduced by the aid of a blower with two storage tanks.
-

- Materials were delivered uniformly into the metal bath, stoppage could not be observed.
- In course of this experiment chemical composition of the metal melt was set by blowing ferro-alloy into the melt.
-
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT85901541T ATE44549T1 (en) | 1984-03-28 | 1985-03-27 | PNEUMATIC LOADING DEVICE FOR FEEDING POWDERY AND GRAINY SUBSTANCES IN METAL METAL. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| HU122484 | 1984-03-28 | ||
| HU122484A HU190268B (en) | 1984-03-28 | 1984-03-28 | Pneumatic feeding device for delivering powder and granular materials into metal fusion |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0178310A1 EP0178310A1 (en) | 1986-04-23 |
| EP0178310B1 true EP0178310B1 (en) | 1989-07-12 |
Family
ID=10953420
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19850901541 Expired EP0178310B1 (en) | 1984-03-28 | 1985-03-27 | Pneumatic charger for feeding pulverized and granular materials into metal melts |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0178310B1 (en) |
| DE (1) | DE3571463D1 (en) |
| HU (1) | HU190268B (en) |
| SU (1) | SU1440338A3 (en) |
| WO (1) | WO1985004416A1 (en) |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ES331393A1 (en) * | 1966-02-02 | 1967-11-16 | Centralny Naoutchno - Issledovetalsky Inst Tch Ornoy Meta | Installation to ensure a good repartition of the scene on the metal in the lingotera of a continuous metal machine. (Machine-translation by Google Translate, not legally binding) |
| DE2105733B2 (en) * | 1971-02-08 | 1975-02-06 | Sueddeutsche Kalkstickstoff-Werke Ag, 8223 Trostberg | Device for removing a fluidizable solid from a pressure vessel |
| DE2248859B2 (en) * | 1972-10-05 | 1975-10-23 | Claudius Peters Ag, 2000 Hamburg | Method and device for the pneumatic conveying of powdery or granular bulk material |
| CH601076A5 (en) * | 1976-08-12 | 1978-06-30 | Battelle Memorial Institute | |
| FR2373469A1 (en) * | 1976-12-10 | 1978-07-07 | Colmant Cuvelier | STORAGE AND EXTRACTION DEVICE FOR PULVERULENT PRODUCTS |
-
1984
- 1984-03-28 HU HU122484A patent/HU190268B/en not_active IP Right Cessation
-
1985
- 1985-03-27 WO PCT/HU1985/000018 patent/WO1985004416A1/en not_active Ceased
- 1985-03-27 EP EP19850901541 patent/EP0178310B1/en not_active Expired
- 1985-03-27 DE DE8585901541T patent/DE3571463D1/en not_active Expired
- 1985-11-25 SU SU853984702A patent/SU1440338A3/en active
Also Published As
| Publication number | Publication date |
|---|---|
| HUT36401A (en) | 1985-09-30 |
| DE3571463D1 (en) | 1989-08-17 |
| WO1985004416A1 (en) | 1985-10-10 |
| EP0178310A1 (en) | 1986-04-23 |
| HU190268B (en) | 1986-08-28 |
| SU1440338A3 (en) | 1988-11-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4883390A (en) | Method and apparatus for effecting pneumatic conveyance of particulate solids | |
| EP0030220B1 (en) | Method for adding solids to molten metal | |
| EP1776301B1 (en) | Device and method for pneumatically conveying bulk materials in a dense flow method | |
| US3260591A (en) | Propelling of addition agents into melts | |
| US4391319A (en) | Apparatus for introducing elements into molten metal streams and casting in inert atmosphere | |
| WO1985004416A1 (en) | Pneumatic charger for feeding pulverized and granular materials into metal melts | |
| DE1583962A1 (en) | Method and device for introducing a finely divided aggregate into molten steel | |
| US6383253B1 (en) | Method for alloying steels and device for carrying out the method | |
| US5173245A (en) | Tuyere injector | |
| GB2106064A (en) | Pneumatic conveyance of solids | |
| SU1440828A1 (en) | Arrangement for pneumatic feed of powder material | |
| US6638337B1 (en) | Method of introducing additives in steelmaking | |
| JPS61115655A (en) | Method for adding low melting metal to molten steel | |
| RU1786100C (en) | Installation for introduction of powdered material in jet of carrier gas into molten metal | |
| JPS61227121A (en) | Apparatus for charging powdery and/or granular material or mixture | |
| WO1997020624A1 (en) | Device for granulating molten metals and slags | |
| CA2283903C (en) | Method for feeding granular solids into metal melts | |
| RU2245832C2 (en) | Method of and device for fixing rates of power material in transport main line | |
| JPS60181218A (en) | Method for blowing powder and granular material at high concentration | |
| SU925815A1 (en) | Device for feeding powder-like materials into molten metal | |
| JP2002521563A (en) | Method for producing zinc by IS method in IS vertical furnace plant and IS vertical furnace plant | |
| SU687134A1 (en) | Method of feeding powder materials to steel melting furnace and device for effectin same | |
| SU1125261A1 (en) | Apparatus for introducing granulated material into metal jet | |
| JPH08618B2 (en) | Method and device for quantitatively taking out gas fluidized powder | |
| DD233361A5 (en) | PNEUMATIC FEEDING DEVICE FOR PROMOTING POWDER AND MATERIAL MATERIALS IN METAL MELTS |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19851121 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE FR GB LI NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19870610 |
|
| R17C | First examination report despatched (corrected) |
Effective date: 19870610 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE FR GB LI NL SE |
|
| REF | Corresponds to: |
Ref document number: 44549 Country of ref document: AT Date of ref document: 19890715 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3571463 Country of ref document: DE Date of ref document: 19890817 |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19900327 Ref country code: AT Effective date: 19900327 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19900328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19900331 Ref country code: CH Effective date: 19900331 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19901001 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19901130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19901201 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| EUG | Se: european patent has lapsed |
Ref document number: 85901541.4 Effective date: 19910110 |