EP0125042B1 - Connectors for power distribution cables - Google Patents
Connectors for power distribution cables Download PDFInfo
- Publication number
- EP0125042B1 EP0125042B1 EP84302476A EP84302476A EP0125042B1 EP 0125042 B1 EP0125042 B1 EP 0125042B1 EP 84302476 A EP84302476 A EP 84302476A EP 84302476 A EP84302476 A EP 84302476A EP 0125042 B1 EP0125042 B1 EP 0125042B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sleeve
- solder
- conductor
- slug
- connector
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
Images


Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01R—ELECTRICALLY-CONDUCTIVE CONNECTIONS; STRUCTURAL ASSOCIATIONS OF A PLURALITY OF MUTUALLY-INSULATED ELECTRICAL CONNECTING ELEMENTS; COUPLING DEVICES; CURRENT COLLECTORS
- H01R4/00—Electrically-conductive connections between two or more conductive members in direct contact, i.e. touching one another; Means for effecting or maintaining such contact; Electrically-conductive connections having two or more spaced connecting locations for conductors and using contact members penetrating insulation
- H01R4/02—Soldered or welded connections
Definitions
- the present invention is directed to connectors for electrical conductors, for example power distribution cables, and methods for use of the connectors.
- connectors refers to connectors that are used both for terminating and for splicing conductors, such as power cables.
- High voltage cables are used for distributing power, and can vary in size from 4 gauge (16 mm 2 ) up to over 3,000 MCM (1500 m m2) .
- compression crimp with a metallic sleeve.
- problems with compression crimps For example, heavy hydraulic crimping tools are required, which can weigh 50 to 100 pounds (22.5 to 45 kgs). These heavy tools are awkward to use in the field.
- a large number of dies are required because a die is needed for each cable size. If the die size is off by even a small fraction, which easily occurs due to die wear, the tool does not perform satisfactorily and crimp failure can result.
- Cadweld Another technique that has been considered is a chemical heating system, known under the tradename Cadweld, for welding conductors together using an exothermic reaction and molten aluminum. This technique has achieved only limited use because it can be dangerous, it involves a gas which needs venting which is difficult in the field, and it is expensive because the molds used wear out after only fifty uses.
- MIG metal inert gas
- US-A-2838592 and US-A-3601783 disclose electrical connector arrangements employing solder-filled connectors wherein an electrical conductor is pushed into the molten solder to effect the connection
- US-A-3 396 460 discloses sleeves which contract to grip the conductors and the solder within the sleeve.
- an electrical connector comprising: at least one tubular sleeve having a closed end and an open end for receiving an electrical conductor within the sleeve, the peripheral inner wall of the sleeve being pretinned, the sleeve being arranged to receive a slug of solder therein proximate to the closed end; and means disposed within the sleeve for exerting pressure on the slug of solder so as to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder melts.
- pretinned means that a surface has been coated with solder or solder-like material such as zinc or bronze.
- solder or solder-like material such as zinc or bronze.
- a single sleeve is used for termination connections and two sleeves in electrically conductive connection are used for splice connections.
- the peripheral inner wall of the sleeve may be pretinned with a solid coating of solder or zinc for example.
- the connector can be provided with the slug of solder in position, preferably proximate to the closed end of the sleeve, or the user of the connector can add the slug of solder in the field.
- a method of connecting a connector to an electrical conductor wherein the connector comprises: at least one tubular sleeve having a closed end and an open end for receiving the electrical conductor within the sleeve, the peripheral inner wall of the sleeve being pretinned, a slug of solder in the sleeve proximate to the closed end of the sleeve, and means disposed within the sleeve for exerting pressure on the slug of solder so as to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder melts; the method comprising placing the electrical conductor into the sleeve of the connector, and heating the solder to at least its melting temperature while simultaneously maintaining the conductor in the sleeve against the force of the pressure-exerting means.
- a method of splicing first and second electrical conductors together by means of an electrically conductive connector that comprises first and second metallic sleeves in electrically conductive connection with each other, each sleeve having a closed end, and an open end for receiving a conductor within the sleeve, the peripheral inner wall of each sleeve being pretinned; a slug of solder in each sleeve proximate to the closed end of the sleeve; and at least in the second sleeve, means disposed within the sleeve for exerting pressure on the slug of solder to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder in the second sleeve melts; the method comprising the steps of connecting the first con- ductorto the connector by placing the first conductor in the first sleeve and heating the first sleeve to a temperature sufficiently high
- the connector of the invention is used in the method of the present invention by heating the sleeve to melt the solder while simultaneously applying a force to relatively move the connector and the conductor toward each other. Until the slug of solder has at least softened, no relative movement between the connector and the conductor is possible. When the solder has melted, the sleeve and the conductor are moved relatively toward each other. The sleeve is continued to be heated and simultaneously the sleeve and conductor are continued to be moved relatively toward each other to extrude solder toward the open end of the sleeve.
- the heating and the moving continue until the conductor can no longer move, i.e., it bottoms out in the connector.
- the size of the slug of solder is chosen so that as the conductor bottoms out, a small portion of the solder is extruded out of the sleeve, which indicates to an operator that connection has been made.
- the conductor and connector are held immobile, while the pressure-exerting means extrudes the solder around the conductor and into the interstices of the conductor.
- the pressure-exerting means produces a force at Tm of at least 10 psi (0.07 MPa), and more preferably at least 30 psi (0.21 MPa), to achieve adequate filling of space between strands.
- the pressure-exerting means produces a force at Tm no greater than 200 psi (1.4 MPa) to prevent the conductor from being forced out of the sleeve.
- Suitable pressure-exerting means are (1) a spring; (2) a heat expandable metal which can be in the form of a spring; (3) a swellable polymer; (4) a gas; (5) a container containing pressurized gas that is released at a temperature greater than 100°Cand uptoTm; (6) reactantsthat evolve a gas, the reactants being separated by a barrier that allows the reactants to react at a temperature greater than 100°C and up to Tm; and (7) reactants that evolve gas when they react, the reactants being reactive only at a temperature between 100°CandTm; and (8) a material that is a fluid at the temperature at which the slug of solder melts, and wherein the connector comprises a sealing memberfor preventing leakage of the fluid past the barrier.
- a connector containing pressure-exerting means can include a metallic barrier between the slug of solder and the pressure-exerting means, the barrier, which may be pretinned, acting as a piston and being dimensionally stable at Tm and axially slidable within the sleeve.
- the barrier may be arranged to melt at a temperature greater than Tm.
- the connector includes sealing means for preventing leakage of the pressure-exerting means past the barrier, particularly when the pressure-exerting means comprises a material that is a fluid at Tm.
- the connector can be provided with a tubular insert for use with conductors that are non-circular in transverse cross-section.
- the tubular insert is metallic, rotatably positioned in the sleeve, and the peripheral inside wall of the insert is pretinned.
- the inside wall of the insert is non-circular in transverse cross-section, having a cross-section that corresponds to the cross-section of the conductor.
- the connector can have a view hole through the wall of the sleeve proximate to the open end of the sleeve for determining when the slug of molten solder has been extruded to a position proximate to the open end of the sleeve.
- inserts of varying wall thickness can be provided, where the peripheral innerwall of each insert is pretinned.
- a flexible metallic sheet coated with solder can be provided. The sheet is wrapped around the conductor until the outer diameter of the wrapped conductor is sufficiently large for the internal diameter of the conductor.
- the connector of the invention may be provided with a mounting hole through the wall of the sleeve for attaching fastening means to the connector for holding an electrical conductor in placing as the pressure-exerting means urges molten solder towards the open end of the sleeve.
- the connector of the invention may be provided with a star-shaped washer positioned proximate the open end of the sleeve with the points of the star extending inwardly such that they grip an electrical conductor inserted in the sleeve.
- This method for making splices or connections is safe, reliable, and easy to use in the field. The only significant piece of equipment required is a torch. The resulting terminations and splices are electrically reliable and physically secure. This method can be used for both aluminum and copper conductors, and also can be used for splicing an aluminum conductor to a copper conductor.
- each tubular sleeve and/or insert used in the invention is metallic.
- the connector and method of the present invention may be used with a stranded or solid conductor, and the conductor may form part of a cable insulated with polymeric material or oil saturated paper.
- the cable may be a multi-conductor sectored cable having conductors that are non-circular in cross-section.
- the connector of the invention will in general be of generally cylindrical configuration, but may, alternatively, be of irregular cross-section.
- the area of a transverse cross-section of the wall of the connector is at least equal to the area of a transverse cross-section through the conductor so that the connector and the conductor have the same capability to conduct electricity. This avoids hot spots in the termination or splice.
- FIG. 3-6 shows a self-activated termination connector provided with means for pressurising molten solder toward the open end of the connector;
- an electrically conductive connector 10 is used for terminating a power cable 12 that comprises insulation 14 that has been cut back to expose a stranded conductor 16.
- the connector 10 comprises a metallic cylindrical tubular sleeve 18 having a closed end 20 and an open end 22.
- the connector 10 is pretinned with a thin, solid coating of solder 24 on the inner peripheral wall 26 of the sleeve 18. There is also a slug of solder 28 in the sleeve proximate to the closed end 20.
- the sleeve 18 is formed from the same material used for the conductor, which in the case of the aluminum conductors can be 1100 series aluminum alloys.
- solder which can be a fluxless solder
- a preferred solder for a copper conductor contains tin, cadmium and zinc, and is available under the tradename Neptune-SS from Rock Mount Research and Alloys, Inc. of Denver, Colorado.
- a preferred fluxless solder for an aluminum conductor contains zinc, aluminum, copper, iron, and magnesium, and is available under the tradename Neptune-S from Rock Mount. Solder used in conjunction with a flux can also be used. In such event, it is preferred to use a multi-cored solder such as for example a solder comprising lead, tin and optionally silver.
- Multi-cored solder typically is an extruded rod of solder containing two or more areas of flux extending longitudinally within the solder rod.
- a multi-cored solder of this type is commercially available from Multi-Cored Solders, Ltd. of Great Britain and under the trademark HMP Solder.
- the thickness of the coating of solder can be in the order of a few tenths of a millimetre (ten thousandths of an inch), and generally is in the order of a few hundredths of a millimetre (thousandths of an inch).
- the pretinning can be achieved by heating the sleeve 10 and melting solder onto the inner peripheral wall 26 or by electroplating.
- the internal diameter of the sleeve 18 must be larger than the outer diameter of the conductor 16, and preferably is at least 12.5x10- 2 mm (5 mils) greater.
- the solder 28 can be pre-placed in the sleeve 18, or the user of the connector can place the solder. When the solder is pre-placed, it can be melted for placement in the sleeve, and when it solidifies it attaches to the walls of the sleeve and securely stays in place.
- the conductor 16 is inserted into the sleeve, bottoming out on the slug 28 of solder. Then the sleeve is heated such as by a torch 30 while simultaneously forcing the connector and the conductor towards each other with a force of at least about 0.07 MPa (10 pounds), preferably at least about 0.21 MPa (30 pounds). When the solder melts, the force results in the sleeve and the conductor moving relatively toward each other. This results in the solder being extruded toward the open end of the sleeve under pressure.
- the pressurized solder fills any interstices in the conductor, including spaces between strands, completely fills the space between the conductor and the sleeve, and fills the closed end of the sleeve as shown by reference number 31 in Fig. 1 B.
- Filling the closed end of the sleeve with solder is important in that it provides good electrical contact between the end of a conductor and the connector. Such contact is absent in a crimp connection.
- the relative movement between the conductor and the solder in a closed environment tends to encourage a metallurgical bond and a high-quality connection.
- any oxide on the conductor is mechanically removed such as with a stainless steel brush before the conductor is inserted into the connector.
- any oxide film on the inner peripheral wall of the sleeve is removed by mechanical abrasion or an ultrasonic technique before pretinning the sleeve to aid in formation of a metallurgical bond between the conductor and the connector.
- the conductor and connector are moved relatively toward each other until the conductor bottoms out in the sleeve and cannot be forced any further. Generally, a small portion of the solder is extruded out of the sleeve as shown by reference numeral 32 in Fig. 18 when bottoming out occurs this helps let the operator know that the connection is complete. The heat is then removed, and the conductor and connector are allowed to cool. This process results in a strong and electrically conductive metallurgical bond between the conductor and the connector.
- the slug of solder has sufficient mass to completely fill any interstices in the conductor, to fill the space between the conductor and the sleeve, and to allow a small portion to be extruded out of the sleeve.
- the sleeve 18 can be formed from a tube that is crimped down to form a closed end 20. With this configuration, there can be an opening toward the closed end.
- An advantage of the present invention is that molten solder is extruded into any openings to close them off.
- the mass 31 of solidified solder stops ingress by water and other contaminants.
- Fig. 2 shows a splice connector 32 according to the present invention that comprises two axially aligned metallic tubular sleeves 44 in electrically conductive connection with each other.
- This connector 32 can be formed from a single metal tube that has a barrier 46 therein.
- the barrier 46 can be held in place by soldering, welding an interference fit, or a press fit.
- Each sleeve 44 is pretinned on its inner peripheral wall with a solid coating 24 of solder and has a slug 28 of solder at its closed end.
- One of the sleeves is shown as having a view hole 46 through its wall so that operator can observe molten solder as it is extruded toward the open end, and stop heating the solder before it extrudes out of the sleeve.
- Only one of the sleeves is shown as having a view hole 46 in Fig. 2, clearly both sleeves can be provided with a view hole.
- the splice connector 42 is used in the same manner as the termination connector 10. That is, each of two conductors is connected to one of the sleeves in the same manner as described above with regard to termination connector 10. The two conductors can be attached to the connector simultaneously, or connection can be done sequentially.
- Splice connectors comprising more than two sleeves can be used.
- splice connectors having three sleeves in the form of a "Y" or “T” can be used, and splice connectors having four sleeves in the form of an "H' can be used.
- Figs. 3-6 show self-activated connectors having means provided for pressurising the solder to the open end of the sleeve when the solder melts.
- the pressurising means is only shown with regard to termination connectors, the pressuring means can be used with one or both sleeves of a splice connector such as the splice connector 32 shown in Fig. 2. As noted above, it is with splice connectors that the pressurising means are most useful. With splice connectors, often once one conductor is connected, it is impossible to have relative movement between the connector and the second conductor. With a self-activated connector, relative movement is not required.
- Figs. 2-6 the same reference numerals are used as in Fig. 1 to show elements that are substantially the same.
- the pressuring means comprises a solid cylinder 52 of a heat swellable or foamable polymer. Between the cylinder 52 and the slug of solder 28 is a barrier or piston 54.
- the piston 54 is axially slidable within the sleeve 18 and is made of a material that is thermally stable and does not melt at the temperature, Tm, at which the slug of solder 28 melts.
- the piston 54 can be made of the same alloy used for the sleeve.
- the piston 54 is pretinned with a coating 55.
- the polymer When heat is applied to the connector 50, the polymer increases in size. Once the slug of solder 28 melts, the polymer forces the piston 54 and the solder 28 toward the open end 22 of the sleeve 18. To prevent the conductor 16 from being forced out of the sleeve, it is held in place by a fastener such as a screw 56 extending through a fastening hole 58 in the wall of the sleeve 18 proximate to the open end 22 of the sleeve.
- a fastener such as a screw 56 extending through a fastening hole 58 in the wall of the sleeve 18 proximate to the open end 22 of the sleeve.
- An alternate approach to prevent conductor "pull out” is the provision of a star-shaped washer about 7.5x10- 2 mm to 12.5x 1 0-2 mmr (3 to 5 mils) thick proximate the open end of the sleeve.
- Such a star-shaped washer has a smooth outer circumference and an inner circumference having a plurality of points.
- the smooth outer surface fits against the inner peripheral wall of the sleeve and the points of the star extend inwardly.
- the points of the star contact and grip the conductor when it is inserted in the sleeve.
- the sharp inner circumference of the washer scrapes the conductor removing any oxide layer that might be present.
- the washer firmly holds the conductor in place and acts as a dam to retain the solder, when molten, within the sleeve.
- a high temperature polymeric sealing sleeve member 60 is provided on the inner peripheral wall of the sleeve 18 adjoining the cylinder 52. As the polymer swells, it forces the sealing member 60 against the inner peripheral wall of the sleeve.
- the piston 54 has a skirt 62 extending toward the closed end 20 of the sleeve 18 and the sealing member 60 is pressured against the inner wall of the skirt 62, thus preventing leakage of the swellable polymer 52 beyond the piston.
- the polymeric sealing member 60 is particularly useful when the pressuring means is a fluid as shown in Figs. 4, 5 and 7.
- the sealing member 60 can be made from a flexible heat- resistant material such as thin aluminum or a polymeric material, preferably a sheet of a polyimide available under the tradename Kapton from DuPont.
- a suitable sleeve can be made from 3 to 4 wraps of 2.5x10- 2 mm (1 mil) thick Kapton.
- the pressurising means produces a force on the piston at Tm, which is generally about 150 to 400°C for solders for aluminum and copper conductors, of at least 0.07 MPa (10 psi), and more preferably at least 0.21 MPa (30 psi) on the piston, to achieve adequate filling of the space between strands and extrude solder all the way toward the open end.
- the pressurising means produces a force at Tm less than 1.4 MPa (200 psi) on the piston to prevent the conductor and the piston from being entirely forced out of the sleeve.
- a preferred material for the polymer contains:
- the foaming agent is available under the tradename Celagen from Uniroyal. Other sulfonyl hydrazide foaming agents can be used.
- suitable polymers can include polyethylene, ethylene vinyl acetate and polypropylene that have been crosslinked by radiation to prevent them from oozing out by the piston 54. Also polymers such as silicone polymers having a foaming agent therein can be used.
- a connector 71 is provided with pressurising means comprising a cylinder 72 containing compressed non-reactive gas 74.
- the cylinder is closed with a solder plug 76.
- the plug of solder 76 melts, thereby releasing the compressed gas 74, which drives the piston 54 and the slug of solder 28, once it is melted, toward the open end of the sleeve.
- a connector 80 has a spring 82 as the pressurising means.
- the spring is made of a material that does not lose its temper at the temperature, Tm, at which the solder melts, i.e., at 360 to 400°C. Suitable materials for the spring 82 include 302 stainless steel, SAE 52100 alloy cabon steel, T1 High speed tool steel, steel alloy 8286 and fnconet 718.
- the spring 82 can be made from a heat-recoverable metal that expands upon heating such as nitinol, a nickel-titanium based alloy available under the trademark Tinel.
- a solder pin 84 is provided.
- the pin 84 extends through two aligned openings 86 in diametrically opposite portions of the sleeve.
- the pin preferably is made of the same solder used for the slug 28 so that when the pin 84 melts, the slug of solder 28 is molten as it is forced by the spring 82 toward the open end of the sleeve.
- a connector 87 can have as pressurising means two reactants 88 and 90 separated by a barrier 92 that melts at a temperature greater than 100°C up to Tm.
- the barrier 92 can be made of solder.
- the reactants can be materials that evolve gas when they react such as sodium bicarbonate and acetic acid.
- the barrier 92 can be eliminated if the reactants do not react or do not exert excessive pressure until reaching an elevated temperature of at least greater than 100°C.
- a powder can be used that releases a gas at an elevated temperature.
- Pressuring means are particularly useful in one or both sleeves of a splice connector having first and second sleeves in electrically conductive connection.
- a first conductor is connected in the first sleeve.
- a second conductor is connected to the connector by placing the second conductor in the second sleeve, heating the slug of solder in the second sleeve to at least Tm while simultaneously maintaining the second conductor in the second sleeve against the force of the pressuring means.
- the pressuring means forces the molten solder toward the open end of the sleeve to completely fill the space between the second conductor and the second sleeve with solder. Thus, it is not necessary to move the second conductor and the connector toward each other after the first conductor is connected.
- Fig. 7 shows a conductor 16 wrapped in a flexible sheet of wrapping 96 so that the conductor 16 can fit into a connector having a sleeve with an internal diameter too large for the unwrapped conductor.
- the wrapping 96 can comprise a flexible metallic sheet having a solid coating of solder on one or both surfaces.
- the wrap can be made of aluminum of about 12.5x10- 2 mm to about 50x10- Z mm (about 5 to about 20 mils) thick with a coating of solder, the same type used for the plug of about 2.5x10- 2 mm to 5x 1 0-2 mm (about 1 to 2 mils) thick.
- the wrap can have markings thereon to identify the length required for conductors of different diameter.
- a kit can be provided comprising a connector and pre- marked wrapping so that a single kit can accommodate a large number of sizes of conductors.
- a connector can be provided with a metallic insert that is pretinned on its inner peripheral surface.
- the splice connector 100 comprises two sleeves 102, one of which is provided with a metallic insert 104 having a solid coating 106 of solder on its inner peripheral surface.
- the insert 104 is rotatably mounted in the sleeve 102.
- the inner wall of the insert is non-circular in transverse cross-section. This allows the connector 100 to be used for conductors that are non-circlar in transverse cross-section, and particularly the conductors of sectored high power cables.
- the insert 104 is rotatable. This allows the insert to be aligned with the conductor so the conductor can be inserted into the insert. Without such a rotatable insert, alignment can be impossible once the splice connector 100 has been connected to a first conductor. After this first connection, it is impossible to rotate the connector to achieve alignment, and often the second conductor cannot be rotated.
- inserts 104, pressuring means, wrapping 90, and view ports 46 can be used alone or in combination, and can be used with both splice connectors and termination connectors.
- kits can contain a pretinned sleeve having a slug of solder therein, or the slug of solder can be provided separately in the kit.
- the kit can have a variety of sizes of slugs of solder to accommodate different sizes of cables.
- the kit can include wrapping, inserts, and fasteners 56.
- the barrier at the "closed" end of a sleeve can be (1) the wall of the sleeve itself as in Fig. 1A; (2) an installed barrier such as barrier 46 in Fig. 2; or (3) can in effect be the piston 28.
- An example of this third version is a self-activated two sleeve splice connector where there is no barrier 46 and a single spring is used to power two pistons, one piston in each sleeve.
- a termination connector 10 having the form shown in Fig. 1A was formed from a tube made of 6061 aluminum alloy that was 112.5 mm (4) inches) long. One end of the tube was crimped closed to produce a sleeve about 50 mm (2 inches) long.
- the sleeve had an internal diameter of 13.67 mm (35/64 inch) and an outer diameter of 18.75 mm (I inch).
- the inner peripheral wall of the sleeve was pretinned with Neptune-S in a thickness of about 1.25xlO-' mm (5 mils)..Sixteen grams of Neptune-S was placed at the closed end of the sleeve.
- the sleeve was used to make a connection with 4 gauge size stranded aluminum conductor by simultaneously pushing the conductor toward the closed end of the sleeve and melting the solder.
- a conventional crimped termination was made at the other end of the conductor. A tensile force was then applied to the assembly. The crimped connection failed while the connection made with the connector 10 held fast.
- the tube had an internal diameter of 13.67 mm (35/64 inch) and an outer diameter of 18.75 mm (42 inch).
- a cylindrical block of 12.5 mm (2 inch) thickness was press fitted into the center of the tube, thereby forming two sleeves, each of which was pretinned with Neptune-S solder.
- a first 4 gauge stranded aluminum conductor was connected to one of the sleeves by simultaneously pushing the conductor toward the closed end of the sleeve while melting the solder therein. Thereafter, a second stranded 4 gauge aluminum conductor was connected to the connector by pushing the conductor toward the closed portion of the second sleeve while simultaneously melting the solder therein.
- a termination connection and a splice connection were made as described in Examples 1 and 2 except the conductors were 1,000 MCM stranded aluminum conductor and the termination connector and splice connector were correspondingly larger.
- Heat cycle tests are currently under way using a heat cycle period of 4 hours on, 2 hours off, a current of 1100 amps and a maximum temperature during each cycle of 130°C. The tests have been under way for three weeks and so far the connections have passed the tests in that the temperature rise of the connections has been substantially the same as the temperature rise of the conductors themselves.
- the resultant connection can handle thermal cycling without failure, remains intact even under high tensile forces, and can be used with cables over 1,000 MCM in size, where crimps often can not be used.
- the barrier 46 can be eliminated from a splice connector, and a single means for pressuring solder such as a spring can be used for simultaneously pressuring both slugs of solder toward both open ends of the connector.
- small diameter cables can be connected to large diameter conductors without using wrapping 96.
- the sleeve has been referred to throughout as being “tubular"
- the sleeve may be made in the form of two (or more) longitudinally split partial sleeves (“clam-shells”), which may be assembled about the conductor(s) to form the tubular sleeve for use.
Landscapes
- Connections Effected By Soldering, Adhesion, Or Permanent Deformation (AREA)
- Coupling Device And Connection With Printed Circuit (AREA)
- Cable Accessories (AREA)
- Insulated Conductors (AREA)
- Details Of Connecting Devices For Male And Female Coupling (AREA)
- Removal Of Insulation Or Armoring From Wires Or Cables (AREA)
- Communication Cables (AREA)
- Multi-Conductor Connections (AREA)
- Organic Insulating Materials (AREA)
- Vessels, Lead-In Wires, Accessory Apparatuses For Cathode-Ray Tubes (AREA)
- Table Devices Or Equipment (AREA)
- Agricultural Chemicals And Associated Chemicals (AREA)
- Processing Of Terminals (AREA)
Abstract
Description
- The present invention is directed to connectors for electrical conductors, for example power distribution cables, and methods for use of the connectors.
- As used herein, the term "connectors" refers to connectors that are used both for terminating and for splicing conductors, such as power cables.
- A variety of techniques have been developed for terminating or splicing high voltage cables in the field. High voltage cables are used for distributing power, and can vary in size from 4 gauge (16 mm2) up to over 3,000 MCM (1500 mm2).
- One technique commonly used is a compression crimp with a metallic sleeve. However, there are problems with compression crimps. For example, heavy hydraulic crimping tools are required, which can weigh 50 to 100 pounds (22.5 to 45 kgs). These heavy tools are awkward to use in the field. In addition, a large number of dies are required because a die is needed for each cable size. If the die size is off by even a small fraction, which easily occurs due to die wear, the tool does not perform satisfactorily and crimp failure can result.
- Another problem with compression crimps is lack of reliability, especially with aluminum conductors. If an unsatisfactory crimp is formed, the termination or splice can overheat which can result in a fire, system failure, and a blackout.
- When a compression crimp is used, often the crimp is filled with a conductive grease to insure better electrical contact and to prevent oxidation. In the field, this conductive grease is very messy. At high temperature the grease can flow resulting in poor electrical contact.
- Another problem noted with compression crimps, particularly for aluminum conductors, is that cold flow occurs due to thermal cycling. This can result in a thermal runaway which can cause a fire.
- Another technique for forming terminations and splices that has been used is sweating, where hot molten solder is poured into the termination or splice. This also is a very difficult technique to use in the field. A hot tub of solder is required, which creates safety hazards and there are significant losses of expensive solder. Further, temperature control is essential to a good splice or termination, and is difficult to achieve in the field. If the temperature is too low, a satisfactory connection does not result due to a poor metallurgical bond. If the temperature is too high, flux in the solder degrades, resulting in a brittle connection which can fail. Hence, there is considerable worker skill required.
- Another technique that has been considered is a chemical heating system, known under the tradename Cadweld, for welding conductors together using an exothermic reaction and molten aluminum. This technique has achieved only limited use because it can be dangerous, it involves a gas which needs venting which is difficult in the field, and it is expensive because the molds used wear out after only fifty uses.
- One further technique that has been considered is metal inert gas (MIG) welding, that is welding the aluminum conductors under inert gas to prevent oxidation of the aluminum. This technique requires expensive equipment which is generally unsuitable for field use in that it weighs several hundred pounds or more and is not easily portable.
- US-A-2838592 and US-A-3601783 disclose electrical connector arrangements employing solder-filled connectors wherein an electrical conductor is pushed into the molten solder to effect the connection, and US-A-3 396 460 discloses sleeves which contract to grip the conductors and the solder within the sleeve.
- In accordance with one aspect of the present invention, there is provided an electrical connector comprising: at least one tubular sleeve having a closed end and an open end for receiving an electrical conductor within the sleeve, the peripheral inner wall of the sleeve being pretinned, the sleeve being arranged to receive a slug of solder therein proximate to the closed end; and means disposed within the sleeve for exerting pressure on the slug of solder so as to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder melts.
- As used herein the term "pretinned" means that a surface has been coated with solder or solder-like material such as zinc or bronze. Although the invention will be discussed below principally with regard to pretinning with solder, it is to be understood that coating other than solder can be used.
- A single sleeve is used for termination connections and two sleeves in electrically conductive connection are used for splice connections.
- The peripheral inner wall of the sleeve may be pretinned with a solid coating of solder or zinc for example.
- The connector can be provided with the slug of solder in position, preferably proximate to the closed end of the sleeve, or the user of the connector can add the slug of solder in the field.
- In accordance with another aspect of the present invention, there is provided a method of connecting a connector to an electrical conductor, wherein the connector comprises: at least one tubular sleeve having a closed end and an open end for receiving the electrical conductor within the sleeve, the peripheral inner wall of the sleeve being pretinned, a slug of solder in the sleeve proximate to the closed end of the sleeve, and means disposed within the sleeve for exerting pressure on the slug of solder so as to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder melts; the method comprising placing the electrical conductor into the sleeve of the connector, and heating the solder to at least its melting temperature while simultaneously maintaining the conductor in the sleeve against the force of the pressure-exerting means.
- In accordance with a still further aspect of the present invention, there is provided a method of splicing first and second electrical conductors together by means of an electrically conductive connector that comprises first and second metallic sleeves in electrically conductive connection with each other, each sleeve having a closed end, and an open end for receiving a conductor within the sleeve, the peripheral inner wall of each sleeve being pretinned; a slug of solder in each sleeve proximate to the closed end of the sleeve; and at least in the second sleeve, means disposed within the sleeve for exerting pressure on the slug of solder to urge the solder towards the open end of the sleeve at the temperature at which the slug of solder in the second sleeve melts; the method comprising the steps of connecting the first con- ductorto the connector by placing the first conductor in the first sleeve and heating the first sleeve to a temperature sufficiently high to melt the slug of solder in the first sleeve; and connecting the second conductor to the connector by placing the second conductor in the second sleeve, heating the slug of solder in the second sleeve to at least the temperature at which the slug of solder melts while simultaneously maintaining the second conductor in the second sleeve against the force of the pressure-exerting means, thereby to force the molten solder towards the open end of the sleeve to fill the space between the second conductor and the second sleeve with solder.
- The connector of the invention is used in the method of the present invention by heating the sleeve to melt the solder while simultaneously applying a force to relatively move the connector and the conductor toward each other. Until the slug of solder has at least softened, no relative movement between the connector and the conductor is possible. When the solder has melted, the sleeve and the conductor are moved relatively toward each other. The sleeve is continued to be heated and simultaneously the sleeve and conductor are continued to be moved relatively toward each other to extrude solder toward the open end of the sleeve. This completely fills any interstices in the conductor, such as spaces between strands of stranded conductors, and also completely fills the space between the conductor and the sleeve with solder. Preferablythe heating and the moving continue until the conductor can no longer move, i.e., it bottoms out in the connector. Preferably the size of the slug of solder is chosen so that as the conductor bottoms out, a small portion of the solder is extruded out of the sleeve, which indicates to an operator that connection has been made.
- In some circumstances, it is not possible to move the sleeve and the conductor toward each other. For instance, when splicing two electrical conductors together, after the first conductor is connected to the connector, the connector can no longer be moved, and often the other conductor is relatively immobile.
- In accordance with one aspect of the invention as set out in
Claim 14, the conductor and connector are held immobile, while the pressure-exerting means extrudes the solder around the conductor and into the interstices of the conductor. - Preferably the pressure-exerting means produces a force at Tm of at least 10 psi (0.07 MPa), and more preferably at least 30 psi (0.21 MPa), to achieve adequate filling of space between strands. Preferably the pressure-exerting means produces a force at Tm no greater than 200 psi (1.4 MPa) to prevent the conductor from being forced out of the sleeve.
- Exemplary of suitable pressure-exerting means are (1) a spring; (2) a heat expandable metal which can be in the form of a spring; (3) a swellable polymer; (4) a gas; (5) a container containing pressurized gas that is released at a temperature greater than 100°Cand uptoTm; (6) reactantsthat evolve a gas, the reactants being separated by a barrier that allows the reactants to react at a temperature greater than 100°C and up to Tm; and (7) reactants that evolve gas when they react, the reactants being reactive only at a temperature between 100°CandTm; and (8) a material that is a fluid at the temperature at which the slug of solder melts, and wherein the connector comprises a sealing memberfor preventing leakage of the fluid past the barrier.
- A connector containing pressure-exerting means, referred to as a "self-activated connector" herein, can include a metallic barrier between the slug of solder and the pressure-exerting means, the barrier, which may be pretinned, acting as a piston and being dimensionally stable at Tm and axially slidable within the sleeve. The barrier may be arranged to melt at a temperature greater than Tm. Preferably the connector includes sealing means for preventing leakage of the pressure-exerting means past the barrier, particularly when the pressure-exerting means comprises a material that is a fluid at Tm.
- The connector can be provided with a tubular insert for use with conductors that are non-circular in transverse cross-section. The tubular insert is metallic, rotatably positioned in the sleeve, and the peripheral inside wall of the insert is pretinned. The inside wall of the insert is non-circular in transverse cross-section, having a cross-section that corresponds to the cross-section of the conductor.
- The connector can have a view hole through the wall of the sleeve proximate to the open end of the sleeve for determining when the slug of molten solder has been extruded to a position proximate to the open end of the sleeve.
- So that a single sleeve can accommodate more than one conductor size, inserts of varying wall thickness can be provided, where the peripheral innerwall of each insert is pretinned. Alternatively, a flexible metallic sheet coated with solder can be provided. The sheet is wrapped around the conductor until the outer diameter of the wrapped conductor is sufficiently large for the internal diameter of the conductor.
- The connector of the invention may be provided with a mounting hole through the wall of the sleeve for attaching fastening means to the connector for holding an electrical conductor in placing as the pressure-exerting means urges molten solder towards the open end of the sleeve.
- The connector of the invention may be provided with a star-shaped washer positioned proximate the open end of the sleeve with the points of the star extending inwardly such that they grip an electrical conductor inserted in the sleeve.
- This method for making splices or connections is safe, reliable, and easy to use in the field. The only significant piece of equipment required is a torch. The resulting terminations and splices are electrically reliable and physically secure. This method can be used for both aluminum and copper conductors, and also can be used for splicing an aluminum conductor to a copper conductor.
- Preferably the or each tubular sleeve and/or insert used in the invention is metallic.
- In arranging for the sleeve to receive the slug of solder, it will be appreciated that the relative size of these components is to be taken into account. The connector and method of the present invention may be used with a stranded or solid conductor, and the conductor may form part of a cable insulated with polymeric material or oil saturated paper. The cable may be a multi-conductor sectored cable having conductors that are non-circular in cross-section.
- The connector of the invention will in general be of generally cylindrical configuration, but may, alternatively, be of irregular cross-section.
- Preferably the area of a transverse cross-section of the wall of the connector is at least equal to the area of a transverse cross-section through the conductor so that the connector and the conductor have the same capability to conduct electricity. This avoids hot spots in the termination or splice.
- Several embodiments of electrical connectors, and connecting and splicing methods, each in accordance with the present invention, will now be described, by way of example, with reference to the accompanying drawings, in which:
- Fig. 1A shows in transverse cross-section a connector being used to terminate a power cable;
- Fig. 1B shows the termination of Fig. 1A;
- Fig. 2 shows in transverse cross-section a splice connector.
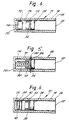
- Each of Figs. 3-6 shows a self-activated termination connector provided with means for pressurising molten solder toward the open end of the connector;
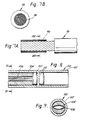
- Fig. 7A is a front elevation view of a power cable where the conductor is wrapped in a pretinned flexible sheet of metal;
- Fig. 7B is a transverse cross-section view of the cable of Fig. 7A taken on line B-B in Fig. 7A;
- Fig. 8 shows in transverse cross-section a splice connector having an insert therein; and
- Fig. 9 is a view of the splice connector of Fig. 8 taken along line 10-10 in Fig. 8.
- With reference to Fig. 1, an electrically
conductive connector 10 is used for terminating apower cable 12 that comprisesinsulation 14 that has been cut back to expose a strandedconductor 16. - As shown in Fig. 1, the
connector 10 comprises a metallic cylindricaltubular sleeve 18 having aclosed end 20 and anopen end 22. - The
connector 10 is pretinned with a thin, solid coating ofsolder 24 on the innerperipheral wall 26 of thesleeve 18. There is also a slug ofsolder 28 in the sleeve proximate to theclosed end 20. - Preferably the
sleeve 18 is formed from the same material used for the conductor, which in the case of the aluminum conductors can be 1100 series aluminum alloys. - The same solder, which can be a fluxless solder, can be used both for the
coating 24 and theslug 28. A preferred solder for a copper conductor contains tin, cadmium and zinc, and is available under the tradename Neptune-SS from Rock Mount Research and Alloys, Inc. of Denver, Colorado. A preferred fluxless solder for an aluminum conductor contains zinc, aluminum, copper, iron, and magnesium, and is available under the tradename Neptune-S from Rock Mount. Solder used in conjunction with a flux can also be used. In such event, it is preferred to use a multi-cored solder such as for example a solder comprising lead, tin and optionally silver. Multi-cored solder typically is an extruded rod of solder containing two or more areas of flux extending longitudinally within the solder rod. A multi-cored solder of this type is commercially available from Multi-Cored Solders, Ltd. of Great Britain and under the trademark HMP Solder. - The thickness of the coating of solder can be in the order of a few tenths of a millimetre (ten thousandths of an inch), and generally is in the order of a few hundredths of a millimetre (thousandths of an inch). The pretinning can be achieved by heating the
sleeve 10 and melting solder onto the innerperipheral wall 26 or by electroplating. - The internal diameter of the
sleeve 18 must be larger than the outer diameter of theconductor 16, and preferably is at least 12.5x10⁻² mm (5 mils) greater. - The
solder 28 can be pre-placed in thesleeve 18, or the user of the connector can place the solder. When the solder is pre-placed, it can be melted for placement in the sleeve, and when it solidifies it attaches to the walls of the sleeve and securely stays in place. - To use the
connector 10, theconductor 16 is inserted into the sleeve, bottoming out on theslug 28 of solder. Then the sleeve is heated such as by atorch 30 while simultaneously forcing the connector and the conductor towards each other with a force of at least about 0.07 MPa (10 pounds), preferably at least about 0.21 MPa (30 pounds). When the solder melts, the force results in the sleeve and the conductor moving relatively toward each other. This results in the solder being extruded toward the open end of the sleeve under pressure. The pressurized solder fills any interstices in the conductor, including spaces between strands, completely fills the space between the conductor and the sleeve, and fills the closed end of the sleeve as shown byreference number 31 in Fig. 1 B. - Filling the closed end of the sleeve with solder is important in that it provides good electrical contact between the end of a conductor and the connector. Such contact is absent in a crimp connection.
- The relative movement between the conductor and the solder in a closed environment tends to encourage a metallurgical bond and a high-quality connection.
- Preferably, any oxide on the conductor is mechanically removed such as with a stainless steel brush before the conductor is inserted into the connector. Preferably any oxide film on the inner peripheral wall of the sleeve is removed by mechanical abrasion or an ultrasonic technique before pretinning the sleeve to aid in formation of a metallurgical bond between the conductor and the connector.
- The conductor and connector are moved relatively toward each other until the conductor bottoms out in the sleeve and cannot be forced any further. Generally, a small portion of the solder is extruded out of the sleeve as shown by
reference numeral 32 in Fig. 18 when bottoming out occurs this helps let the operator know that the connection is complete. The heat is then removed, and the conductor and connector are allowed to cool. This process results in a strong and electrically conductive metallurgical bond between the conductor and the connector. - The slug of solder has sufficient mass to completely fill any interstices in the conductor, to fill the space between the conductor and the sleeve, and to allow a small portion to be extruded out of the sleeve.
- The
sleeve 18 can be formed from a tube that is crimped down to form aclosed end 20. With this configuration, there can be an opening toward the closed end. An advantage of the present invention is that molten solder is extruded into any openings to close them off. Themass 31 of solidified solder stops ingress by water and other contaminants. - Fig. 2 shows a
splice connector 32 according to the present invention that comprises two axially aligned metallictubular sleeves 44 in electrically conductive connection with each other. Thisconnector 32 can be formed from a single metal tube that has abarrier 46 therein. Thebarrier 46 can be held in place by soldering, welding an interference fit, or a press fit. Eachsleeve 44 is pretinned on its inner peripheral wall with asolid coating 24 of solder and has aslug 28 of solder at its closed end. - One of the sleeves is shown as having a
view hole 46 through its wall so that operator can observe molten solder as it is extruded toward the open end, and stop heating the solder before it extrudes out of the sleeve. Although only one of the sleeves is shown as having aview hole 46 in Fig. 2, clearly both sleeves can be provided with a view hole. - The splice connector 42 is used in the same manner as the
termination connector 10. That is, each of two conductors is connected to one of the sleeves in the same manner as described above with regard totermination connector 10. The two conductors can be attached to the connector simultaneously, or connection can be done sequentially. - Splice connectors comprising more than two sleeves can be used. For example, splice connectors having three sleeves in the form of a "Y" or "T" can be used, and splice connectors having four sleeves in the form of an "H' can be used.
- Figs. 3-6 show self-activated connectors having means provided for pressurising the solder to the open end of the sleeve when the solder melts. Although the pressurising means is only shown with regard to termination connectors, the pressuring means can be used with one or both sleeves of a splice connector such as the
splice connector 32 shown in Fig. 2. As noted above, it is with splice connectors that the pressurising means are most useful. With splice connectors, often once one conductor is connected, it is impossible to have relative movement between the connector and the second conductor. With a self-activated connector, relative movement is not required. - In Figs. 2-6, the same reference numerals are used as in Fig. 1 to show elements that are substantially the same.
- In Fig. 3, the pressuring means comprises a
solid cylinder 52 of a heat swellable or foamable polymer. Between thecylinder 52 and the slug ofsolder 28 is a barrier orpiston 54. Thepiston 54 is axially slidable within thesleeve 18 and is made of a material that is thermally stable and does not melt at the temperature, Tm, at which the slug ofsolder 28 melts. Thepiston 54 can be made of the same alloy used for the sleeve. Preferably thepiston 54 is pretinned with acoating 55. - When heat is applied to the connector 50, the polymer increases in size. Once the slug of
solder 28 melts, the polymer forces thepiston 54 and thesolder 28 toward theopen end 22 of thesleeve 18. To prevent theconductor 16 from being forced out of the sleeve, it is held in place by a fastener such as ascrew 56 extending through afastening hole 58 in the wall of thesleeve 18 proximate to theopen end 22 of the sleeve. An alternate approach to prevent conductor "pull out" is the provision of a star-shaped washer about 7.5x10⁻² mm to 12.5x 1 0-2 mmr (3 to 5 mils) thick proximate the open end of the sleeve. Such a star-shaped washer has a smooth outer circumference and an inner circumference having a plurality of points. When positioned in the sleeve the smooth outer surface fits against the inner peripheral wall of the sleeve and the points of the star extend inwardly. The points of the star contact and grip the conductor when it is inserted in the sleeve. As the conductor is forced into the connector the sharp inner circumference of the washer scrapes the conductor removing any oxide layer that might be present. In addition, the washer firmly holds the conductor in place and acts as a dam to retain the solder, when molten, within the sleeve. - To prevent the polymer from leaking out around the
piston 54, a high temperature polymeric sealingsleeve member 60 is provided on the inner peripheral wall of thesleeve 18 adjoining thecylinder 52. As the polymer swells, it forces the sealingmember 60 against the inner peripheral wall of the sleeve. Thepiston 54 has askirt 62 extending toward theclosed end 20 of thesleeve 18 and the sealingmember 60 is pressured against the inner wall of theskirt 62, thus preventing leakage of theswellable polymer 52 beyond the piston. The polymeric sealingmember 60 is particularly useful when the pressuring means is a fluid as shown in Figs. 4, 5 and 7. The sealingmember 60 can be made from a flexible heat- resistant material such as thin aluminum or a polymeric material, preferably a sheet of a polyimide available under the tradename Kapton from DuPont. A suitable sleeve can be made from 3 to 4 wraps of 2.5x10⁻² mm (1 mil) thick Kapton. - Preferably the pressurising means produces a force on the piston at Tm, which is generally about 150 to 400°C for solders for aluminum and copper conductors, of at least 0.07 MPa (10 psi), and more preferably at least 0.21 MPa (30 psi) on the piston, to achieve adequate filling of the space between strands and extrude solder all the way toward the open end. Preferably the pressurising means produces a force at Tm less than 1.4 MPa (200 psi) on the piston to prevent the conductor and the piston from being entirely forced out of the sleeve.
- A preferred material for the polymer contains:
- (Parts by weight) Low density polyethylene 80
pbw Ethylene ethylacrylate 20 pbw Hindered phenol antioxidant 0.5 pbw p-Oxy bis(benzene sulfonyl - hydrazide) (foaming agent) 2 pbw
- The foaming agent is available under the tradename Celagen from Uniroyal. Other sulfonyl hydrazide foaming agents can be used.
- Other suitable polymers can include polyethylene, ethylene vinyl acetate and polypropylene that have been crosslinked by radiation to prevent them from oozing out by the
piston 54. Also polymers such as silicone polymers having a foaming agent therein can be used. - With reference to Fig. 4, a
connector 71 is provided with pressurising means comprising acylinder 72 containing compressednon-reactive gas 74. The cylinder is closed with a solder plug 76. As the connector 70 is heated, the plug of solder 76 melts, thereby releasing the compressedgas 74, which drives thepiston 54 and the slug ofsolder 28, once it is melted, toward the open end of the sleeve. - With reference to Fig. 5, a connector 80 has a
spring 82 as the pressurising means. The spring is made of a material that does not lose its temper at the temperature, Tm, at which the solder melts, i.e., at 360 to 400°C. Suitable materials for thespring 82 include 302 stainless steel, SAE 52100 alloy cabon steel, T1 High speed tool steel, steel alloy 8286 and fnconet 718. Thespring 82 can be made from a heat-recoverable metal that expands upon heating such as nitinol, a nickel-titanium based alloy available under the trademark Tinel. - To hold the
piston 28 in place in the version of the invention shown in Fig. 5, asolder pin 84 is provided. Thepin 84 extends through two alignedopenings 86 in diametrically opposite portions of the sleeve. The pin preferably is made of the same solder used for theslug 28 so that when thepin 84 melts, the slug ofsolder 28 is molten as it is forced by thespring 82 toward the open end of the sleeve. - As shown in Fig. 6, a connector 87 can have as pressurising means two
reactants barrier 92 that melts at a temperature greater than 100°C up to Tm. Thebarrier 92 can be made of solder. The reactants can be materials that evolve gas when they react such as sodium bicarbonate and acetic acid. Once the connector 87 is heated and thebarrier 92 melts, thereactants piston 54 and the slug ofsolder 28 toward the open end of the sleeve once the slug of solder has melted. - The
barrier 92 can be eliminated if the reactants do not react or do not exert excessive pressure until reaching an elevated temperature of at least greater than 100°C. - Also a powder can be used that releases a gas at an elevated temperature.
- Pressuring means are particularly useful in one or both sleeves of a splice connector having first and second sleeves in electrically conductive connection. With such a connector, a first conductor is connected in the first sleeve. Then, a second conductor is connected to the connector by placing the second conductor in the second sleeve, heating the slug of solder in the second sleeve to at least Tm while simultaneously maintaining the second conductor in the second sleeve against the force of the pressuring means. The pressuring means forces the molten solder toward the open end of the sleeve to completely fill the space between the second conductor and the second sleeve with solder. Thus, it is not necessary to move the second conductor and the connector toward each other after the first conductor is connected.
- Fig. 7 shows a
conductor 16 wrapped in a flexible sheet of wrapping 96 so that theconductor 16 can fit into a connector having a sleeve with an internal diameter too large for the unwrapped conductor. The wrapping 96 can comprise a flexible metallic sheet having a solid coating of solder on one or both surfaces. The wrap can be made of aluminum of about 12.5x10⁻² mm to about 50x10-Z mm (about 5 to about 20 mils) thick with a coating of solder, the same type used for the plug of about 2.5x10⁻² mm to 5x 1 0-2 mm (about 1 to 2 mils) thick. The wrap can have markings thereon to identify the length required for conductors of different diameter. Thus, a kit can be provided comprising a connector and pre- marked wrapping so that a single kit can accommodate a large number of sizes of conductors. - A connector can be provided with a metallic insert that is pretinned on its inner peripheral surface. With reference to Fig. 8, the
splice connector 100 comprises twosleeves 102, one of which is provided with ametallic insert 104 having asolid coating 106 of solder on its inner peripheral surface. Theinsert 104 is rotatably mounted in thesleeve 102. As shown in Fig. 9, the inner wall of the insert is non-circular in transverse cross-section. This allows theconnector 100 to be used for conductors that are non-circlar in transverse cross-section, and particularly the conductors of sectored high power cables. - An important feature is that the
insert 104 is rotatable. This allows the insert to be aligned with the conductor so the conductor can be inserted into the insert. Without such a rotatable insert, alignment can be impossible once thesplice connector 100 has been connected to a first conductor. After this first connection, it is impossible to rotate the connector to achieve alignment, and often the second conductor cannot be rotated. - Different features of the present invention described above can be used alone or in combination. For example, inserts 104, pressuring means, wrapping 90, and
view ports 46 can be used alone or in combination, and can be used with both splice connectors and termination connectors. - The components needed to make a connection according to the present invention can be provided as a kit. For example, a kit can contain a pretinned sleeve having a slug of solder therein, or the slug of solder can be provided separately in the kit. Further, the kit can have a variety of sizes of slugs of solder to accommodate different sizes of cables. Further, the kit can include wrapping, inserts, and
fasteners 56. - It should be realized that the barrier at the "closed" end of a sleeve can be (1) the wall of the sleeve itself as in Fig. 1A; (2) an installed barrier such as
barrier 46 in Fig. 2; or (3) can in effect be thepiston 28. An example of this third version is a self-activated two sleeve splice connector where there is nobarrier 46 and a single spring is used to power two pistons, one piston in each sleeve. - These and other features of the present invention will be become better understood with reference to the following examples.
- A
termination connector 10 having the form shown in Fig. 1A was formed from a tube made of 6061 aluminum alloy that was 112.5 mm (4) inches) long. One end of the tube was crimped closed to produce a sleeve about 50 mm (2 inches) long. The sleeve had an internal diameter of 13.67 mm (35/64 inch) and an outer diameter of 18.75 mm (I inch). The inner peripheral wall of the sleeve was pretinned with Neptune-S in a thickness of about 1.25xlO-' mm (5 mils)..Sixteen grams of Neptune-S was placed at the closed end of the sleeve. - The sleeve was used to make a connection with 4 gauge size stranded aluminum conductor by simultaneously pushing the conductor toward the closed end of the sleeve and melting the solder.
- A conventional crimped termination was made at the other end of the conductor. A tensile force was then applied to the assembly. The crimped connection failed while the connection made with the
connector 10 held fast. - A splice connector 42 having the configuration shown in Fig. 2, except without a
view hole 46, was made from a 112.5 mm (4) inches) long tube made of aluminum 6061 alloy. The tube had an internal diameter of 13.67 mm (35/64 inch) and an outer diameter of 18.75 mm (42 inch). A cylindrical block of 12.5 mm (2 inch) thickness was press fitted into the center of the tube, thereby forming two sleeves, each of which was pretinned with Neptune-S solder. A slug of Neptune-S solder weighing 16 grams was placed at the closed portion of each sleeve. A first 4 gauge stranded aluminum conductor was connected to one of the sleeves by simultaneously pushing the conductor toward the closed end of the sleeve while melting the solder therein. Thereafter, a second stranded 4 gauge aluminum conductor was connected to the connector by pushing the conductor toward the closed portion of the second sleeve while simultaneously melting the solder therein. - A termination connection and a splice connection were made as described in Examples 1 and 2 except the conductors were 1,000 MCM stranded aluminum conductor and the termination connector and splice connector were correspondingly larger. Heat cycle tests are currently under way using a heat cycle period of 4 hours on, 2 hours off, a current of 1100 amps and a maximum temperature during each cycle of 130°C. The tests have been under way for three weeks and so far the connections have passed the tests in that the temperature rise of the connections has been substantially the same as the temperature rise of the conductors themselves.
- From the above description, it is apparent that significant advantages compared to prior art techniques are obtained from use of the connectors and the method of the present invention. For example, the method is safe, and requires no bulky equipment, only using a simple torch. The connectors are easy to use and connections formed are not craft sensitive. Moreover, connections can be made even with cables having insulation formed from oil saturated paper.
- The resultant connection can handle thermal cycling without failure, remains intact even under high tensile forces, and can be used with cables over 1,000 MCM in size, where crimps often can not be used.
- Although the present invention has been described in considerable detail with reference to certain preferred versions thereof, other versions are possible. For example, the
barrier 46 can be eliminated from a splice connector, and a single means for pressuring solder such as a spring can be used for simultaneously pressuring both slugs of solder toward both open ends of the connector. Further, small diameter cables can be connected to large diameter conductors without using wrapping 96. Also, although the sleeve has been referred to throughout as being "tubular", the sleeve may be made in the form of two (or more) longitudinally split partial sleeves ("clam-shells"), which may be assembled about the conductor(s) to form the tubular sleeve for use.
Claims (17)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT84302476T ATE36095T1 (en) | 1983-04-11 | 1984-04-11 | CONNECTOR FOR POWER DISTRIBUTION CABLE. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US48399783A | 1983-04-11 | 1983-04-11 | |
| US483997 | 1983-04-11 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0125042A1 EP0125042A1 (en) | 1984-11-14 |
| EP0125042B1 true EP0125042B1 (en) | 1988-07-27 |
Family
ID=23922313
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP84302476A Expired EP0125042B1 (en) | 1983-04-11 | 1984-04-11 | Connectors for power distribution cables |
Country Status (17)
| Country | Link |
|---|---|
| EP (1) | EP0125042B1 (en) |
| JP (1) | JPS59209283A (en) |
| AT (1) | ATE36095T1 (en) |
| AU (1) | AU573581B2 (en) |
| BR (1) | BR8401700A (en) |
| CA (1) | CA1224855A (en) |
| DE (1) | DE3473098D1 (en) |
| DK (1) | DK162550C (en) |
| ES (1) | ES8605128A1 (en) |
| FI (1) | FI80969C (en) |
| GB (1) | GB2137913B (en) |
| HU (1) | HU189106B (en) |
| IL (1) | IL71479A (en) |
| MX (1) | MX154854A (en) |
| MY (1) | MY102619A (en) |
| NO (1) | NO166905C (en) |
| ZA (1) | ZA842644B (en) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA1217254A (en) * | 1984-04-27 | 1987-01-27 | Raychem Corporation | Heat activatable sealing piston |
| NL8501258A (en) * | 1985-05-03 | 1986-12-01 | Philips Nv | ELECTRIC MACHINE. |
| GB9404415D0 (en) * | 1994-03-08 | 1994-04-20 | Starpoint Electrics Ltd | Electrical assemblies |
| DE19908031B4 (en) * | 1999-02-24 | 2009-08-13 | Auto-Kabel Management Gmbh | Connection of an electrical aluminum cable with a connector made of copper or the like metal |
| CN107302142A (en) * | 2017-06-30 | 2017-10-27 | 云南科威液态金属谷研发有限公司 | Low-melting-point metal cable connecting arrangement and its application method, attachment structure |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB659113A (en) * | 1948-03-30 | 1951-10-17 | Stackpole Carbon Co | Improvements in or relating to carbon brush structures for use in dynamo electric machines |
| US2838593A (en) * | 1950-02-23 | 1958-06-10 | Scesa Olindo | Connector for electric wires |
| US3221387A (en) * | 1962-06-19 | 1965-12-07 | Vitramon Inc | Terminal lead connection and method of making the same |
| BE635318A (en) * | 1962-07-23 | |||
| DE1216754B (en) * | 1963-05-03 | 1966-05-12 | Ici Ltd | Graphite anode |
| GB1006396A (en) * | 1964-06-09 | 1965-09-29 | Ici Ltd | Electrical conductor |
| US3402758A (en) * | 1966-06-08 | 1968-09-24 | Western Electric Co | Method for die-casting electrical connections |
| AT274947B (en) * | 1967-01-14 | 1969-10-10 | Schunk & Ebe Gmbh | Process for establishing a connection between the cable and the carbon brush of electrical machines |
| US3601783A (en) * | 1969-03-05 | 1971-08-24 | Amp Inc | Electrical connector with spring biased solder interface |
| US3665367A (en) * | 1969-08-20 | 1972-05-23 | Martin Marietta Corp | Side hole terminal |
| US3578896A (en) * | 1969-10-10 | 1971-05-18 | Thomas & Betts Corp | Electrical connector with fusible plug means and heating material |
| US3676575A (en) * | 1970-10-12 | 1972-07-11 | Babcock & Wilcox Co | Brazeable terminal body |
| JPS541031A (en) * | 1977-06-03 | 1979-01-06 | Ricoh Co Ltd | Transfer sheet for copying a large number of elefctrophotographic sheets |
-
1984
- 1984-04-09 IL IL71479A patent/IL71479A/en unknown
- 1984-04-10 NO NO841419A patent/NO166905C/en unknown
- 1984-04-10 DK DK185684A patent/DK162550C/en not_active IP Right Cessation
- 1984-04-10 ES ES531457A patent/ES8605128A1/en not_active Expired
- 1984-04-10 FI FI841414A patent/FI80969C/en not_active IP Right Cessation
- 1984-04-10 ZA ZA842644A patent/ZA842644B/en unknown
- 1984-04-10 AU AU26709/84A patent/AU573581B2/en not_active Ceased
- 1984-04-10 CA CA000451675A patent/CA1224855A/en not_active Expired
- 1984-04-11 JP JP59073867A patent/JPS59209283A/en active Pending
- 1984-04-11 AT AT84302476T patent/ATE36095T1/en active
- 1984-04-11 EP EP84302476A patent/EP0125042B1/en not_active Expired
- 1984-04-11 GB GB08409369A patent/GB2137913B/en not_active Expired
- 1984-04-11 HU HU841422A patent/HU189106B/en unknown
- 1984-04-11 MX MX200973A patent/MX154854A/en unknown
- 1984-04-11 DE DE8484302476T patent/DE3473098D1/en not_active Expired
- 1984-04-11 BR BR8401700A patent/BR8401700A/en not_active IP Right Cessation
-
1987
- 1987-09-30 MY MYPI87002518A patent/MY102619A/en unknown
Also Published As
| Publication number | Publication date |
|---|---|
| ES531457A0 (en) | 1985-10-01 |
| GB2137913A (en) | 1984-10-17 |
| HU189106B (en) | 1986-06-30 |
| AU573581B2 (en) | 1988-06-16 |
| NO166905B (en) | 1991-06-03 |
| ES8605128A1 (en) | 1985-10-01 |
| NO841419L (en) | 1984-10-12 |
| IL71479A (en) | 1987-08-31 |
| GB2137913B (en) | 1986-11-05 |
| AU2670984A (en) | 1984-10-18 |
| DK162550C (en) | 1992-04-06 |
| DK185684D0 (en) | 1984-04-10 |
| HUT35114A (en) | 1985-05-28 |
| MX154854A (en) | 1987-12-21 |
| JPS59209283A (en) | 1984-11-27 |
| FI80969C (en) | 1990-08-10 |
| BR8401700A (en) | 1984-11-20 |
| IL71479A0 (en) | 1984-07-31 |
| DK185684A (en) | 1984-10-12 |
| FI841414L (en) | 1984-10-12 |
| FI841414A0 (en) | 1984-04-10 |
| DE3473098D1 (en) | 1988-09-01 |
| CA1224855A (en) | 1987-07-28 |
| ZA842644B (en) | 1985-11-27 |
| EP0125042A1 (en) | 1984-11-14 |
| DK162550B (en) | 1991-11-11 |
| ATE36095T1 (en) | 1988-08-15 |
| MY102619A (en) | 1992-08-17 |
| FI80969B (en) | 1990-04-30 |
| NO166905C (en) | 1991-09-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4634213A (en) | Connectors for power distribution cables | |
| EP0707321B1 (en) | Braided cable having a solidified end portion | |
| US8802987B2 (en) | Electric wire equipped with terminal fitting and method of manufacturing the same | |
| CA2182461C (en) | Electrical connector and method of making | |
| EP0108518B1 (en) | Apparatus for protection of a substrate | |
| CA1264074A (en) | Cable connection | |
| EP0172072B1 (en) | Solder connector device | |
| US4315175A (en) | Aluminum-to-copper transition member for aluminum wound motors and aluminum wound motor equipped with the same | |
| US4889506A (en) | Solder delivery device | |
| CA1310090C (en) | Electrical terminal and methods of making and using same | |
| EP2625746B1 (en) | System and method for terminating aluminum conductors | |
| JP2013505542A (en) | Electrical terminal connection with molded seal | |
| US4241498A (en) | Device and method for terminating a flat cable | |
| EP0405561B1 (en) | Means for terminating and sealing electrical conductors | |
| CA1224855A (en) | Connectors for power distribution cables | |
| CA1321059C (en) | Methods of terminating and sealing electrical conductor means | |
| US4553809A (en) | Electrical connector | |
| EP0886340A1 (en) | Cable joint | |
| US4518445A (en) | Method for making electrical cables | |
| US3783487A (en) | Cable splice apparatus | |
| US5298101A (en) | Method of welding together cable insulation | |
| CN118399295A (en) | High-compression solid strain clamp | |
| Toyama et al. | Development of the Wiring System Technology to Realize its Weight-Reduction in Vehicles | |
| CN111697404B (en) | High voltage cable tin foil grounding lead cold connection method | |
| US4334122A (en) | Bimetallic electrical connector and method for making such connector |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19840424 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH DE FR IT LI NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19860820 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: RAYCHEM CORPORATION (A DELAWARE CORPORATION) |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE FR IT LI NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19880727 |
|
| REF | Corresponds to: |
Ref document number: 36095 Country of ref document: AT Date of ref document: 19880815 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3473098 Country of ref document: DE Date of ref document: 19880901 |
|
| ITF | It: translation for a ep patent filed | ||
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| ITTA | It: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19920408 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19920416 Year of fee payment: 9 Ref country code: CH Payment date: 19920416 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19920430 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19920514 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 19920604 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19930412 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19930430 Ref country code: CH Effective date: 19930430 Ref country code: BE Effective date: 19930430 |
|
| BERE | Be: lapsed |
Owner name: RAYCHEM CORP. Effective date: 19930430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19931101 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19931229 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19940101 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| EUG | Se: european patent has lapsed |
Ref document number: 84302476.1 Effective date: 19931110 |