CN219324689U - Aviation hydraulic conduit flaring clamping device - Google Patents
Aviation hydraulic conduit flaring clamping device Download PDFInfo
- Publication number
- CN219324689U CN219324689U CN202320071493.2U CN202320071493U CN219324689U CN 219324689 U CN219324689 U CN 219324689U CN 202320071493 U CN202320071493 U CN 202320071493U CN 219324689 U CN219324689 U CN 219324689U
- Authority
- CN
- China
- Prior art keywords
- fixed
- screw rod
- chuck
- movable
- seat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003825 pressing Methods 0.000 claims abstract description 10
- 230000006835 compression Effects 0.000 claims description 5
- 238000007906 compression Methods 0.000 claims description 5
- 238000010586 diagram Methods 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 3
- 238000000034 method Methods 0.000 description 3
- 230000005540 biological transmission Effects 0.000 description 2
- 238000013459 approach Methods 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000009987 spinning Methods 0.000 description 1
Images





Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02T—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO TRANSPORTATION
- Y02T50/00—Aeronautics or air transport
- Y02T50/40—Weight reduction
Landscapes
- Gripping Jigs, Holding Jigs, And Positioning Jigs (AREA)
Abstract
The utility model provides an aviation hydraulic conduit flaring clamping device which comprises a base, wherein a chute is arranged in the middle of the top of the base, one end of the chute is fixedly provided with a fixing seat, and the top of the fixing seat is provided with a fixing chuck; the other end of the chute is provided with a movable seat in a limiting sliding manner through a pressing plate, and the top of the movable seat is provided with a movable chuck; a clamping die assembly for clamping the guide pipe and the flat nozzle is arranged between the fixed chuck and the movable chuck in a matched manner; the screw rod is rotatably installed in the fixed chuck through the screw rod limiting assembly, a threaded section of the screw rod and a nut seat fixed in the movable seat are screwed, and a handle is installed at the tail end of the screw rod. The device adopts a structure type of a fixed chuck and a movable chuck, and eliminates repeated positioning errors during repeated clamping.
Description
Technical Field
The utility model belongs to the field of aviation manufacturing and maintenance process equipment, and particularly relates to an aviation hydraulic conduit flaring clamping device.
Background
The traditional aviation hydraulic conduit flaring clamp is mainly in a positive and negative thread transmission mode, and two movable chucks are in a two-way movement clamping type structure, but due to errors such as a thread fit clearance, clamp assembly and debugging precision and the like, an inner hole of the clamp is not concentric with a main shaft of a flaring machine, positioning precision is poor during multiple clamping, and further problems that a conduit conical surface after flaring is not concentric with a tube body deflection, the conical surface is uneven, surface quality is poor and the like occur.
Disclosure of Invention
In order to solve the technical problems, the utility model provides an aviation hydraulic conduit flaring clamping device, which adopts a structural type of a fixed chuck and a movable chuck, eliminates repeated positioning errors during repeated clamping, clamps the fixed chuck and the movable chuck according to working states after being integrally fixed on a machine tool during clamp manufacturing, installs a boring cutter on a main shaft of a flaring machine, self-bores inner holes of the fixed chuck and the movable chuck through equipment, can ensure high precision coaxiality of the inner holes of the chucks and the main shaft of the machine tool, eliminates threads and assembly gaps through locking bolts after clamping the chucks, and is applicable to conduits of different specifications by adopting a replaceable bushing.
In order to achieve the technical characteristics, the aim of the utility model is realized in the following way: the flaring clamping device of the aviation hydraulic conduit comprises a base, wherein a chute is arranged in the middle of the top of the base, one end of the chute is fixedly provided with a fixing seat, and the top of the fixing seat is provided with a fixing chuck; the other end of the chute is provided with a movable seat in a limiting sliding manner through a pressing plate, and the top of the movable seat is provided with a movable chuck; a clamping die assembly for clamping the guide pipe and the flat nozzle is arranged between the fixed chuck and the movable chuck in a matched manner; the screw rod is rotatably installed in the fixed chuck through the screw rod limiting assembly, a threaded section of the screw rod and a nut seat fixed in the movable seat are screwed, and a handle is installed at the tail end of the screw rod.
The fixing seat is fixed at the top end of the base through the compression bolt and the cylindrical locating pin.
The clamp plate is fixed on the top of base through a plurality of compression screws.
The clamping die assembly comprises an inner hole which is processed on the inner side walls of the fixed chuck and the movable chuck, a replaceable bushing is arranged in the inner hole, and a stepped hole is processed in the middle of the end face of the replaceable bushing; the replaceable bushing is positioned and installed in the pin holes of the fixed chuck and the movable chuck through corresponding bolts.
The screw rod limiting assembly comprises a first thrust ball bearing and a second thrust ball bearing which are arranged in the fixing seat, and the outer end of the first thrust ball bearing is fixed in a limiting manner through a gasket, a stop gasket and a round nut which are arranged at the end head of the screw rod; the outer end of the second thrust ball bearing is limited and fixed through a collar on the screw rod.
The movable seat is provided with a locking bolt for locking and positioning the movable seat.
The utility model has the following beneficial effects:
1. the utility model provides an aviation hydraulic conduit flaring clamping device which adopts a structure type of a fixed chuck and a movable chuck, and can eliminate repeated positioning errors during repeated clamping.
2. When the fixture is manufactured, after the fixture is integrally fixed on a machine tool, the chuck of the fixture is clamped according to the working state, a boring cutter is arranged on a main shaft of a flaring machine, and the inner hole of the chuck is self-bored by equipment, so that the high-precision coaxiality of the inner hole of the chuck and the main shaft of the machine tool can be ensured.
3. The clamping head is clamped, threads and assembly gaps are eliminated through the locking bolt, and the replaceable bushing is suitable for the guide pipes with different specifications, so that the flaring precision of the guide pipes can be remarkably improved.
4. The clamping device has the advantages of high clamping and positioning precision, stable work, simple operation, convenient use, safety, reliability and the like.
Drawings
The utility model is further described below with reference to the drawings and examples.
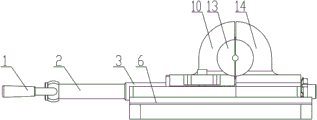
Fig. 1 is a front view of the present utility model.
Fig. 2 is a right side view of the present utility model.
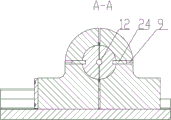
Fig. 3 is a view A-A of fig. 2 in accordance with the present utility model.
Fig. 4 is a view B-B of fig. 2 in accordance with the present utility model.
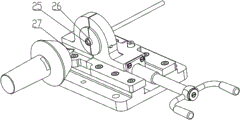
Fig. 5 is a first perspective three-dimensional view of the present utility model.
Fig. 6 is a second perspective three-dimensional view of the present utility model.
Fig. 7 is a three-dimensional view of a third perspective of the present utility model.
Fig. 8 is a diagram of the clamping state of the device according to the utility model during use.
Fig. 9 is a state diagram of the device of the present utility model after flaring is completed.
Fig. 10 is a diagram showing the state before flaring of the catheter and the flat nozzle.
Fig. 11 is a state diagram after flaring of the catheter and flat nozzle.
In the figure: the device comprises a handle 1, a screw rod 2, a pressing plate 3, a threaded section 4, a sliding groove 5, a base 6, a nut seat 7, a movable seat 8, a pin hole 9, a movable chuck 10, an inner hole 11, a stepped hole 12, a replaceable bushing 13, a fixed chuck 14, a fixed seat 15, a stop washer 16, a round nut 17, a cylindrical positioning pin 18, a locking bolt 19, a washer 20, a first thrust ball bearing 21, a second thrust ball bearing 22, a collar 23, a plug 24, a guide pipe 25, a flat pipe nozzle 26 and a flaring cone 27.
Detailed Description
Embodiments of the present utility model will be further described with reference to the accompanying drawings.
Referring to fig. 1-11, an aviation hydraulic conduit flaring clamping device comprises a base 6, wherein a chute 5 is arranged in the middle of the top of the base 6, one end of the chute 5 is fixedly provided with a fixing seat 15, and the top of the fixing seat 15 is provided with a fixing chuck 14; the other end of the chute 5 is provided with a movable seat 8 in a limiting sliding manner through a pressing plate 3, and the top of the movable seat 8 is provided with a movable chuck 10; a clamping die assembly for clamping the guide pipe 25 and the flat nozzle 26 is cooperatively arranged between the fixed chuck 14 and the movable chuck 10; the screw rod 2 is rotatably mounted in the fixed clamping head 14 through a screw rod limiting assembly, a threaded section 4 of the screw rod 2 and a nut seat 7 fixed in the movable seat 8 are fixedly arranged in the screw rod, and the handle 1 is mounted at the tail end of the screw rod 2. The device adopts the structural style of a fixed chuck and a movable chuck, eliminates repeated positioning errors during repeated clamping, clamps the fixed chuck and the movable chuck of the clamp according to working states after being integrally fixed on a machine tool during clamp manufacturing, installs a boring cutter on a main shaft of a flaring machine, self-bores inner bores of the fixed chuck and the movable chuck through equipment, can ensure high precision coaxiality of the inner bores of the chucks and the main shaft of the machine tool, eliminates threads and assembly gaps through a locking bolt after clamping the chucks, adopts a replaceable bushing to be suitable for catheters with different specifications, can obviously improve the flaring precision of the catheters, and has the advantages of high clamping positioning precision, stable work, simplicity in operation, convenience in use, safety, reliability and the like.
Further, the fixing base 15 is fixed at the top end of the base 6 through a compression bolt and a cylindrical positioning pin 18. The fixing seat 15 can be positioned through the cylindrical positioning pin 18, so that the installation precision of the fixing seat is ensured.
Further, the pressing plate 3 is fixed at the top end of the base 6 through a plurality of pressing screws. The pressing plate 3 can be used for limiting the movable seat 8, so that the movable seat can slide along the sliding groove 5, and the falling danger is prevented.
Further, the clamping die assembly comprises an inner hole 11 processed on the inner side walls of the fixed chuck 14 and the movable chuck 10, a replaceable bushing 13 is arranged in the inner hole 11, and a stepped hole 12 is processed in the middle of the end face of the replaceable bushing 13; the replaceable bushings 13 are positioned and mounted inside the pin holes 9 of the fixed 14 and movable 10 jaws by corresponding pins 24. The clamping die assembly is mainly used for clamping and fixing the conduit 25 to be flared and the flat nozzle 26, so that the conduit 25 is conveniently subjected to subsequent flaring operation by adopting a flaring cone and a machine tool. In the specific clamping process, the flat nozzle 26 is arranged inside the inner holes 11 of the fixed chuck 14 and the movable chuck 10, so that the flat nozzle 26 is clamped, and after the flat nozzle is clamped, the conduit 25 inside the flat nozzle 26 is flared through the flaring cone.
The inner hole 11 is processed by firstly mounting the whole fixture on a machine tool, self-boring the inner holes 11 of the fixed chuck and the movable chuck by equipment, and the inner holes are not moved after self-boring, so that the high-precision coaxiality of the fixed chuck and the movable chuck is damaged after the self-boring.
Further, the screw rod limiting assembly comprises a first thrust ball bearing 21 and a second thrust ball bearing 22 which are arranged in the fixed seat 15, and the outer end of the first thrust ball bearing 21 is fixedly limited by a washer 20, a stop washer 16 and a round nut 17 which are arranged at the end head of the screw rod 2; the outer end of the second thrust ball bearing 22 is limited and fixed through a collar 23 on the screw rod 2. The screw rod limiting assembly can ensure that the screw rod can smoothly rotate under the action of the handle 2 and can bear axial force, and further the screw rod limiting assembly is used for driving the movable seat 8 to smoothly slide along the sliding groove, so that clamping action is realized.
Further, a locking bolt 19 for locking and positioning the movable seat 8 is mounted on the movable seat. The locking bolt 19 is used for eliminating threads and assembly gaps, and the replaceable bushing is suitable for catheters with different specifications, so that the flaring precision of the catheters can be remarkably improved.
The assembly and use process of the utility model is as follows:
when the flaring of the catheter is needed, firstly, assembling the catheter and a flat nozzle, sleeving the flat nozzle at the end part of the catheter, then, arranging the flat nozzle inside the inner holes 11 of the fixed chuck 14 and the movable chuck 10, manually rotating the screw rod 2, driving the threaded section 4 through the screw rod 2, driving the nut seat 7 through the threaded section 4, driving the movable seat 8 through the nut seat 7, driving the movable chuck 10 through the movable seat 8, then, matching the movable chuck 10 with the fixed chuck 14, further clamping and fixing the flat nozzle 26, and removing threads and assembly gaps through locking screws after clamping the chucks; the machine tool is started, the main shaft drives the flaring cone, and the conduit 25 is flared through the flaring cone.
The principle of the utility model is as follows:
1. the aviation hydraulic conduit flaring machine is usually reformed by adopting a common horizontal lathe, a flaring clamp is generally arranged on a middle carriage of the lathe, a flaring cone is arranged on a main shaft of the lathe, a conduit is clamped on the flaring clamp, the lathe is started firstly during flaring operation, the main shaft drives the flaring cone to rotate, a large carriage of the manual operation lathe moves along a longitudinal guide rail, the conduit approaches the flaring cone and gradually exerts force, and conical flaring of the conduit is realized through spinning of the flaring cone.
2. The fixed chuck is fixed and fixed with the base through a cylindrical locating pin, and is fastened through a compression screw.
3. The movable chuck is in threaded fit with the screw rod for transmission, and the movable chuck can move along the axis of the screw rod by rotating the screw rod.
4. The movable clamp is provided with a screw hole, a set screw is arranged on the movable clamp, the movable clamp is tightly propped up by rotating the set screw after being clamped by the clamp, and threads and assembly gaps are eliminated.
5. Two unidirectional thrust ball bearings are arranged on the screw rod and used for reducing friction force when the screw rod rotates.
6. The round nut at the end of the screw rod is loose-proof by adopting a stop washer, and when the round nut is fastened, a gap of 0.1mm is reserved in the axial direction of the screw rod, so that the screw rod can be flexibly rotated.
7. When the product is installed with a flaring machine tool, a hinge pin hole is formed in a cylindrical pin hole on the base, a cylindrical pin is installed for positioning, and a bolt is installed in a bolt hole for compressing and fastening.
8. When the fixture is manufactured, after the fixture is integrally fixed on a machine tool, the chuck of the fixture is clamped according to the working state, a boring cutter is arranged on a main shaft of a flaring machine, and the inner hole of the chuck is self-bored by equipment, so that the high-precision coaxiality of the inner hole of the chuck and the main shaft of the machine tool can be ensured.
9. The replaceable bushings with different specifications and sizes are matched, and the replaceable bushings are adopted to be suitable for the guide pipes with different specifications.
Claims (6)
1. An aviation hydraulic conduit flaring clamping device which is characterized in that: the device comprises a base (6), wherein a chute (5) is arranged in the middle of the top of the base (6), a fixed seat (15) is fixedly arranged at one end of the chute (5), and a fixed clamping head (14) is arranged at the top of the fixed seat (15); the other end of the chute (5) is provided with a movable seat (8) in a limiting sliding manner through a pressing plate (3), and the top of the movable seat (8) is provided with a movable chuck (10); a clamping die assembly for clamping the guide pipe (25) and the flat nozzle (26) is cooperatively arranged between the fixed chuck (14) and the movable chuck (10); the screw rod (2) is rotatably arranged in the fixed clamping head (14) through the screw rod limiting assembly, a threaded section (4) of the screw rod (2) and a nut seat (7) fixed in the movable seat (8), and a handle (1) is arranged at the tail end of the screw rod (2).
2. An aircraft hydraulic duct flare clamping device as in claim 1, wherein: the fixing seat (15) is fixed at the top end of the base (6) through a compression bolt and a cylindrical locating pin (18).
3. An aircraft hydraulic duct flare clamping device as in claim 1, wherein: the pressing plate (3) is fixed at the top end of the base (6) through a plurality of pressing screws.
4. An aircraft hydraulic duct flare clamping device as in claim 1, wherein: the clamping die assembly comprises an inner hole (11) which is processed on the inner side walls of a fixed chuck (14) and a movable chuck (10), a replaceable bushing (13) is arranged in the inner hole (11), and a stepped hole (12) is processed in the middle of the end face of the replaceable bushing (13); the replaceable bushing (13) is positioned and installed inside the pin holes (9) of the fixed clamping head (14) and the movable clamping head (10) through corresponding bolts (24).
5. An aircraft hydraulic duct flare clamping device as in claim 1, wherein: the screw rod limiting assembly comprises a first thrust ball bearing (21) and a second thrust ball bearing (22) which are arranged in the fixed seat (15), and the outer end of the first thrust ball bearing (21) is limited and fixed through a gasket (20), a stop washer (16) and a round nut (17) which are arranged at the end head of the screw rod (2); the outer end of the second thrust ball bearing (22) is limited and fixed through a collar (23) on the screw rod (2).
6. An aircraft hydraulic duct flare clamping device as in claim 1, wherein: the movable seat (8) is provided with a locking bolt (19) for locking and positioning the movable seat.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202320071493.2U CN219324689U (en) | 2023-01-10 | 2023-01-10 | Aviation hydraulic conduit flaring clamping device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202320071493.2U CN219324689U (en) | 2023-01-10 | 2023-01-10 | Aviation hydraulic conduit flaring clamping device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN219324689U true CN219324689U (en) | 2023-07-11 |
Family
ID=87064116
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202320071493.2U Active CN219324689U (en) | 2023-01-10 | 2023-01-10 | Aviation hydraulic conduit flaring clamping device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN219324689U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117282865A (en) * | 2023-11-24 | 2023-12-26 | 星箭中航(成都)机械制造有限公司 | Self-aligning concentric flaring device |
-
2023
- 2023-01-10 CN CN202320071493.2U patent/CN219324689U/en active Active
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117282865A (en) * | 2023-11-24 | 2023-12-26 | 星箭中航(成都)机械制造有限公司 | Self-aligning concentric flaring device |
| CN117282865B (en) * | 2023-11-24 | 2024-02-20 | 星箭中航(成都)机械制造有限公司 | Self-aligning concentric flaring device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109014267A (en) | A kind of fixed device of thin-walled parts aeroelasticity with threaded hole | |
| CN102490056B (en) | Tooth surface locating and finish turning fixture for bevel planet gear | |
| CN109079204A (en) | A kind of engine nozzle ring inclined-hole jig | |
| CN211708192U (en) | Equal-division milling machine for pipe barrel parts | |
| CN117282865B (en) | Self-aligning concentric flaring device | |
| CN110328547B (en) | Positioning and clamping composite device for processing differential mechanism shell assembly | |
| CN110756866A (en) | A thin-walled cylindrical piece drilling inclined hole clamping device and its operation method | |
| CN220006885U (en) | Edge milling fixing clamp for spray pipe seat | |
| CN113894740A (en) | Quick-change auxiliary tool for pressing sleeve of shell bushing | |
| CN211101739U (en) | A thin-walled cylindrical part drilling inclined hole clamping device | |
| CN220718534U (en) | Quick location is with cover that rises | |
| CN217317076U (en) | Self-centering clamping mechanism for shaft parts | |
| CN114083264B (en) | Reducing rolling riveting installation tool for knuckle bearing | |
| CN214601998U (en) | Can dismantle fast from centering chuck | |
| CN210588288U (en) | Positioning and clamping composite device for machining differential mechanism shell assembly | |
| CN221087885U (en) | Special assembly lathe | |
| CN209578930U (en) | A New Type of Fully Automatic Rotating Device for Lathe | |
| CN221210155U (en) | Tool for screw thread repair | |
| CN223776038U (en) | Inner circle fine-tuning tightening device | |
| CN119703789B (en) | Turning, milling, drilling, boring, honing, broaching composite machine tool and machining process | |
| CN116511359B (en) | A self-centering expansion tool for an expansion-type catheter end | |
| CN113799018A (en) | Self-positioning mechanism for precisely aligning semi-ring parts | |
| CN116765260A (en) | Aviation large-diameter stainless steel conduit flaring processing method | |
| CN221984477U (en) | Tool for machining throttle pipe on A320 main landing gear | |
| CN223531793U (en) | A manual welding internal support clamp |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |