CN219155870U - Device for mould stacking and automatic stacking system - Google Patents
Device for mould stacking and automatic stacking system Download PDFInfo
- Publication number
- CN219155870U CN219155870U CN202223598607.3U CN202223598607U CN219155870U CN 219155870 U CN219155870 U CN 219155870U CN 202223598607 U CN202223598607 U CN 202223598607U CN 219155870 U CN219155870 U CN 219155870U
- Authority
- CN
- China
- Prior art keywords
- stacking
- conveyor
- mould
- driving assembly
- bearing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 230000007246 mechanism Effects 0.000 claims abstract description 101
- 238000006073 displacement reaction Methods 0.000 abstract description 3
- 238000010924 continuous production Methods 0.000 abstract description 2
- 238000010586 diagram Methods 0.000 description 8
- 230000006872 improvement Effects 0.000 description 7
- 230000003028 elevating effect Effects 0.000 description 5
- 238000000034 method Methods 0.000 description 5
- 238000004519 manufacturing process Methods 0.000 description 4
- 230000008569 process Effects 0.000 description 4
- 230000004048 modification Effects 0.000 description 3
- 238000012986 modification Methods 0.000 description 3
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000001174 ascending effect Effects 0.000 description 1
- 230000005540 biological transmission Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
Images




Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P40/00—Technologies relating to the processing of minerals
- Y02P40/50—Glass production, e.g. reusing waste heat during processing or shaping
- Y02P40/57—Improving the yield, e-g- reduction of reject rates
Landscapes
- Stacking Of Articles And Auxiliary Devices (AREA)
Abstract
The utility model discloses a device for mould stacking and an automatic stacking system, wherein the device comprises: the lifting mechanism and the bearing mechanism are used for bearing the die; the lifting mechanism comprises a mounting bracket and a first driving assembly, and the mounting bracket is arranged at the side part of the conveyor; the bearing mechanism is arranged on the mounting bracket, when the die is stacked, the bearing mechanism can convey the die into the goods shelf without horizontal displacement, the output end of the first driving assembly is connected with the bearing mechanism, and the bearing mechanism is driven by the first driving assembly to reciprocate along the mounting bracket and the inside of the goods shelf so as to realize the die stacking to the preset stacking position on the goods shelf. The utility model also discloses an automatic stacking system comprising the device. The automatic stacking device has the advantages of compact structure, safety, reliability, stable operation, high automation degree and the like, realizes accurate stacking of the dies into the goods shelves, and meets the requirement of automatic continuous production.
Description
Technical Field
The utility model belongs to the technical field of prefabricated mold stacking, and particularly relates to a device for mold stacking and an automatic stacking system.
Background
At present, when stacking/unstacking the concrete-filled die in the multi-layer goods shelf, a mode that a cantilever stacker goes in and out of the multi-layer goods shelf is generally adopted. The cantilever stacker crane can enter the inside of a set layer of the multi-layer shelf for unstacking/stacking when unstacking/stacking, and then exit the layer of shelf after unstacking/stacking of the layer of shelf is completed, and enter the next layer of shelf for working. The working mode of going back and forth to get in and out the goods shelves can't satisfy required work efficiency when the production beat is very fast, wastes time and energy moreover, and intensity of labour is big.
Disclosure of Invention
The utility model aims to solve the technical problem of overcoming the defects of the prior art and providing a device for die stacking and an automatic stacking system, which have the advantages of compact structure, safety, reliability, stable operation and high degree of automation.
In order to solve the technical problems, the utility model adopts the following technical scheme:
an apparatus for mold stacking, comprising: the lifting mechanism and the bearing mechanism are used for bearing the die; the lifting mechanism comprises a mounting bracket and a first driving assembly, and the mounting bracket is arranged at the side part of the conveyor; the bearing mechanism is arranged on the mounting bracket, the output end of the first driving assembly is connected with the bearing mechanism, and the bearing mechanism is driven by the first driving assembly to lift reciprocally along the mounting bracket and the inside of the goods shelf so as to realize the stacking of the mould to the preset stacking position on the goods shelf.
As a further improvement of the utility model, the lifting mechanism spans the ends of adjacent conveyors in a "gate" type configuration.
As a further improvement of the utility model, a group of lifting mechanisms are symmetrically arranged at two sides of the conveyor along the running direction of the conveyor, and bearing mechanisms are arranged at two sides of the conveyor.
As a further improvement of the utility model, the bearing mechanism comprises a bearing table and a second driving component, wherein the bearing table is provided with a roller, and the second driving component is used for driving the roller to rotate so as to realize the movement of the die on the bearing table.
As a further improvement of the utility model, the bearing table is of a straight-line structure, and the roller is arranged on the outer side of the bearing table.
As a further improvement of the present utility model, the carrying mechanism further includes: the device comprises a first mounting plate, a second mounting plate and a first pulley; the bearing table is arranged on the second mounting plate and is used for bearing the die; the end of the first mounting plate is connected with the second mounting plate, the first pulley is mounted on the side of the second mounting plate, and driven by the first driving assembly, the first pulley slides back and forth along the inner side of the mounting bracket so as to realize the reciprocating lifting of the bearing mechanism. As a further development of the utility model, the carrier means further comprise a suspension loop, which is located on the carrier table or the first mounting plate for connection to the first drive assembly.
As a further improvement of the utility model, the lifting mechanism further comprises a first guide rail; the first guide rail is arranged on the inner side of the mounting bracket, the first pulley is positioned in the first guide rail, and the first pulley carries out reciprocating lifting sliding along the first guide rail under the driving of the first driving assembly.
As a further improvement of the utility model, the lifting mechanism further comprises a rotating shaft and a inhaul cable, the output end of the first driving component is connected with the rotating shaft, one end of the inhaul cable is wound on the rotating shaft, the other end of the inhaul cable is connected with the bearing mechanism, and the inhaul cable drives the bearing mechanism to lift reciprocally along the mounting bracket under the driving of the first driving component.
As a general technical concept, the utility model also discloses an automatic stacking system, which comprises the device for stacking the moulds, a conveyor for conveying racks and the moulds and a lifting conveying table for lifting the conveyor and the moulds to a preset stacking height, wherein the device for stacking the moulds is arranged between adjacent conveyors and is used for assisting the moulds to be automatically stacked in the racks on the conveyor.
Compared with the prior art, the utility model has the advantages that:
1. according to the device for stacking the dies, the mounting bracket is arranged on the side part of the conveyor, the bearing mechanism is arranged on the mounting bracket of the lifting mechanism, the output end of the driving assembly is connected with the bearing mechanism, the driving assembly is used for providing driving force, the bearing mechanism is lifted up and down reciprocally along the mounting bracket, the dies are lifted up and down vertically to the stacking position preset on the goods shelf, the dies can be stacked or unstacked in the goods shelf only by lifting up and down reciprocally, the horizontal displacement is not needed, the working efficiency is greatly improved, and the requirement of continuous automatic production is well met.
2. According to the device for stacking the molds, the lifting mechanisms are arranged at the two sides of the adjacent conveyor in the mode of being in the shape of the door and transversely arranged at the end parts of the adjacent conveyor or symmetrically arranged along the running direction of the conveyor, so that convenience in stacking the molds is improved, safe running of the conveyor is not affected, and working efficiency of stacking the molds is remarkably improved.
3. According to the device for stacking the dies, the roller is arranged on the bearing table of the bearing mechanism, and the running state of the roller is precisely controlled through the driving assembly, so that the structure arrangement of the bearing table is effectively simplified, and meanwhile, the stability and safety of the dies in the carrying and stacking processes are improved.
4. According to the automatic stacking system, the lifting conveying table is utilized to lift the conveyor and the die to the preset stacking height, the device for stacking the die is arranged between the adjacent conveyors, and the automatic conveying and automatic stacking of the die into the goods shelf are realized through the assistance of the device for stacking the die, so that the structural arrangement of the automatic stacking system is simplified, the efficiency of die conveying and stacking is greatly improved, and the requirement of automatic continuous production is well met.
Drawings
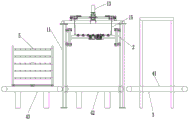
Fig. 1 is a schematic diagram of a front view structure of an automatic stacking system in embodiment 1 of the present utility model.
Fig. 2 is a schematic side view of the automatic stacking system in embodiment 1 of the present utility model.
Fig. 3 is a schematic top view of the automatic stacking system in embodiment 1 of the present utility model.
Fig. 4 is a schematic diagram of a front view of a bearing mechanism in an apparatus for stacking molds according to embodiment 1 of the present utility model.
Fig. 5 is a schematic side view of a carrying mechanism in the apparatus for stacking molds according to embodiment 1 of the present utility model.
Fig. 6 is a schematic top view of a loading mechanism in the apparatus for stacking molds according to embodiment 1 of the present utility model.
Fig. 7 is a schematic diagram of a front view of an automatic stacking system according to embodiment 2 of the present utility model.
Fig. 8 is a schematic side view of the automatic stacking system in embodiment 2 of the present utility model.
Fig. 9 is a schematic top view of the automatic stacking system in embodiment 2 of the present utility model.
Fig. 10 is a schematic diagram of a front view of a bearing mechanism in an apparatus for stacking molds according to embodiment 2 of the present utility model.
Fig. 11 is a schematic side view of a carrying mechanism in the apparatus for stacking molds according to embodiment 2 of the present utility model.
Fig. 12 is a schematic top view of a loading mechanism in the apparatus for stacking molds according to embodiment 2 of the present utility model.
Fig. 13 is a schematic view of lifting a carrying mechanism to a stacking height in embodiment 3 of the present utility model.
Fig. 14 is a schematic diagram of a conveyor transporting a pallet into a palletizing zone after the lifting table lifts the mold to a palletizing height in embodiment 3 of the present utility model.
Fig. 15 is a schematic view of the carrying mechanism in embodiment 3 of the present utility model after the carrying mechanism descends to a certain height and the lifting conveying table lifts the mold to a stacking height and then cooperates with the conveying mold to enter the shelf.
Fig. 16 is a schematic view of the carrying mechanism in embodiment 3 of the present utility model after receiving the mold and descending to the stacking height of the next layer.
Fig. 17 is a schematic diagram of a carrying mechanism exiting a palletizing zone after palletizing of the entire pallet in embodiment 3 of the present utility model.
Fig. 18 is a schematic view of the lifting of the carrying mechanism to the stacking height in embodiment 4 of the present utility model.
Fig. 19 is a schematic view of a carrier descending by a certain height after a pallet enters a palletizing zone in embodiment 4 of the present utility model.
Fig. 20 is a schematic diagram of a carrying mechanism in embodiment 4 of the present utility model after a lifting conveying table is lifted to a stacking height by lowering a certain height to match with a conveying die to enter a shelf.
Fig. 21 is a schematic view of the carrying mechanism of embodiment 4 of the present utility model after receiving a mold and descending to the stacking height of the next layer.
Fig. 22 is a schematic diagram of a carrying mechanism exiting a palletizing zone after palletizing the entire pallet according to embodiment 4 of the present utility model.
Legend description: 1. a lifting mechanism; 11. a mounting bracket; 12. a first guide rail; 13. a first drive assembly; 14. a rotating shaft; 15. a guy cable; 2. a carrying mechanism; 21. a carrying platform; 22. a second drive assembly; 23. a first mounting plate; 24. a second mounting plate; 25. a first pulley; 26. a roller; 27. hanging lugs; 28. a mounting frame; 3. lifting the conveying table; 4. a conveyor; 41. a first conveyor; 42. a second conveyor; 43. a third conveyor; 5. a goods shelf; 51. a bracket; 6. and (5) a mold.
Detailed Description
The utility model is further described below in connection with the drawings and the specific preferred embodiments, but the scope of protection of the utility model is not limited thereby.
Example 1
As shown in fig. 1 to 6, the apparatus for mold stacking of the present utility model includes: a lifting mechanism 1 and a bearing mechanism 2 for bearing a mould 6. The lifting mechanism 1 comprises a mounting bracket 11, a first driving assembly 13, a rotating shaft 14 and a guy rope 15, wherein the mounting bracket 11 spans across the two sides of the conveyor 4. The bearing mechanism 2 is arranged on the mounting bracket 11, when stacking is carried out, the bearing mechanism 2 can convey the die 7 into the goods shelf 5 without horizontal displacement, the output end of the first driving component 13 is connected with the rotating shaft 14, one end of the inhaul cable 15 is wound on the rotating shaft 14, the other end of the inhaul cable is connected with the bearing mechanism 2, and under the driving of the first driving component 13, the inhaul cable 15 drives the bearing mechanism 2 to reciprocate along the mounting bracket 11 and the inner space of the goods shelf 5, so that the die 6 is stacked to a preset stacking position on the goods shelf 5. Specifically, in the stacking process, the carrying mechanism 2 is lifted up and down along the mounting bracket 11 and is lifted up and down in the channel inside the goods shelf 5, and the carrying mechanism 2 and the goods shelf 5 share a space to pass through up and down, so that the effect of completing continuous multi-layer stacking without transversely moving the carrying mechanism 2 to draw out the goods shelf 5 is achieved. It can be appreciated that in this embodiment, the first driving assembly 13 may specifically be a servo motor, or may be another driving mechanism, so long as the bearing mechanism 2 and the mold 6 can be driven to stably lift. The guy cable 15 may specifically take the form of a steel rope or a chain, as long as the bearing mechanism 2 and the die 6 can be pulled to stably lift.
In this embodiment, through setting up the mechanism 2 that bears on the installing support 11 of elevating system 1, and be connected with the mechanism 2 that bears with the output of first drive assembly 13 through pivot 14 and cable 15, utilize first drive assembly 13 to provide the drive power, realized bearing mechanism 2 and carry out reciprocal lift along installing support 11, just also realized mould 6 and go up and down to the pile up neatly position of predetermineeing on the goods shelves in vertical direction, only need reciprocal lift can realize mould 6 pile up neatly or the stack in goods shelves 5, work efficiency has been improved greatly, continuous type automated production's demand has been satisfied well. Further, through adopting cable 15 to come the transmission drive power, realized more accurate control bear mechanism 2 in the ascending travel distance of vertical, improved the precision of mould 6 pile, and then improved the security and the stability of mould 6 pile.
As shown in fig. 1 to 3, in the present embodiment, the lifting mechanism 1 spans the end portions of the adjacent conveyors 4 in a "gate" type structure. Namely, the device for stacking the molds plays a role of a bridge between the adjacent conveyors 4, so that the molds 6 conveyed by one conveyor 4 are smoothly stacked into the goods shelves 5 placed on the other conveyor 4, and a mechanism for enabling the bearing mechanism 2 to move or stretch and slide is not required to be additionally arranged.
As shown in fig. 4 to 6, in the present embodiment, the carrying mechanism 2 includes a carrying table 21 and a second driving assembly 22, a mounting frame 28 is provided on the carrying table 21, a roller 26 is provided on the mounting frame 28, and the second driving assembly 22 is used for driving the roller 26 to rotate so as to move the mold 6 on the carrying table 21. It will be appreciated that in this embodiment, the second driving assembly 22 may be a servo motor, or may be another driving mechanism, so long as the roller 26 can be driven to roll smoothly.
Further, the carrying platform 21 has a straight-line structure, and the rollers 26 are disposed at two outer sides of the carrying platform 21. By arranging the bearing table 21 in the bearing mechanism 2 into a straight-line structure, the structure arrangement of the bearing table 21 is effectively simplified, and meanwhile, the stability and the safety of the die 6 in the carrying and stacking processes are improved. As shown in fig. 3, in this embodiment, in order to improve the stacking efficiency of the molds, multiple brackets 51 are disposed in parallel on opposite sides of the shelf 5, so as to cooperate with the carrying table 21 to more rapidly stack the molds 6 into the shelf 5, so that the carrying mechanism 2 can complete the stacking operation of the multi-layer shelf by only carrying out corresponding lifting movement in the shelf 5, which is rapid and efficient.
As shown in fig. 4 to 6, in the present embodiment, the carrying mechanism 2 further includes: a first mounting plate 23, a second mounting plate 24 and a first pulley 25; the bearing table 21 is mounted on the second mounting plate 24 and is used for bearing the die 6; the both ends of first mounting panel 23 are connected with second mounting panel 24 respectively, and the top both sides of first mounting panel 23 are equipped with the hangers 27 that are used for connecting cable 15, and first pulley 25 is installed in second mounting panel 24 lateral part, under the drive of first drive assembly 13, and cable 15 pulls first pulley 25 and carries out reciprocating sliding along installing support 11 inboard to realize bearing mechanism 2 reciprocal lift.
Specifically, the first mounting plates 23 are arranged along the horizontal direction, and the two second mounting plates 24 are arranged at two ends of the first mounting plates 23 in parallel along the vertical direction, namely, two ends of the second mounting plates 24 are connected through the first mounting plates 23, so that all the first pulleys 25 on the second mounting plates 24 are ensured to synchronously move, and further stable lifting of the bearing table 21 is realized.
As shown in fig. 2, in this embodiment, a first guide rail 12 is disposed inside the mounting bracket 11, a first pulley 25 is located in the first guide rail 12, and the first pulley 25 is driven by the first driving assembly 13 to reciprocate along the first guide rail 12. The pulley and guide rail matched moving mode is adopted, and the device has the advantages of being simple in structure, convenient and fast to move, accurate in moving distance control and the like.
It can be appreciated that in this embodiment, the first driving assembly 13 and the second driving assembly 22 may be connected to an external control system, for example, a PLC control system, and the first driving assembly 13 and the second driving assembly 22 are controlled to automatically operate by using the external control system, so that automatic stacking of the molds can be realized, which is convenient and efficient.
Example 2
As shown in fig. 7 to 12, the apparatus for mold stacking of the present utility model is similar in structural arrangement and operation to the apparatus for mold stacking of embodiment 1, except that: the lifting mechanisms 1 are symmetrically arranged on two sides of the conveyor 4 along the running direction of the conveyor 4, and the bearing mechanisms 2 are arranged on two sides of the conveyor 4. Namely, the conveyor 4 is wrapped on the inner side of the die stacking device, and the bearing mechanism 2 bears from the two sides of the die 7, so that the safety and the stability of the die 7 in the process of carrying and stacking are ensured. As shown in fig. 9, in this embodiment, in order to improve the efficiency of stacking the molds, a plurality of brackets 51 are disposed in parallel on both outer sides of the pallet 5, so as to more quickly stack the molds 6 into the pallet 5 in cooperation with the carrying table 21 and smoothly move down onto another layer of pallet.
Example 3
As shown in fig. 13 to 17, the automatic stacking system of the present utility model includes the device for mold stacking in embodiment 1, the first conveyor 41 for conveying the racks 5, the second conveyor 42 for conveying the molds 6, and the elevating conveyor table 3 for elevating the second conveyor 42 and the molds 6 to a preset stacking height, the device for mold stacking being provided between the adjacent first conveyor 41 and second conveyor 42 for assisting the automatic stacking of the molds 6 into the racks 5 on the first conveyor 41.
According to the automatic stacking system, when stacking is carried out, the bearing mechanism 2 is driven by the lifting mechanism 1 to be lifted to a set stacking height. At the same time, the first conveyor 41 conveys the pallet 5 to above the carrying mechanism 2 and enters a palletizing state. After the carrying mechanism 2 lifts the second conveyor 42 and the die 5 to a set height by the lifting conveying table 3, the carrying mechanism 2 is matched with the second conveyor 42 to convey the die 6 into the goods shelf 5, the carrying mechanism 2 is lowered to the next stacking height after carrying the die 5, and the next plate die is conveyed into a cage by the lifting conveying table 3 and the second conveyor 42. The carrying mechanism 2 is lifted and lowered in the designed channel of the goods shelf 5 until the goods shelf 5 is full of moulds. After the mould is filled, the first conveyor 41 conveys the pallet 5 out of the palletizing zone.
In this embodiment, through setting up the device that is used for mould pile between adjacent conveyer 4, realized the automatic transportation of mould 6 and automatic pile in goods shelves 5, not only simplified the structure setting of automatic pile system, improved the efficiency of mould 6 transport and pile moreover greatly, satisfied the demand of automatic continuous type production well.
Example 4
The automatic stacking system of the present utility model includes the device for mold stacking in embodiment 2, the third conveyor 43 for conveying the racks 5 onto the second conveyor 42, the first conveyor 41 for conveying the molds 6, and the elevating conveyor table 3 for elevating the first conveyor 41 and the molds 6 to a preset stacking height, the device for mold stacking being provided outside the second conveyor 42 for assisting the automatic stacking of the molds 6 into the racks 5 on the second conveyor 42.
As shown in fig. 18 to 22, when stacking, the carrying mechanism 2 is lifted to a set stacking height under the driving of the lifting mechanism 1, and the third conveyor 43 conveys the shelf 5 onto the second conveyor 42 to enter a stacking state. After the lifting conveying table 3 lifts the first conveyor 41 and the die 5 to a set height, the bearing mechanism 2 is matched with the first conveyor 41 to convey the die 6 into the goods shelf 5, the bearing mechanism 2 is lowered to the next stacking height after bearing the die 5, and the next plate die is conveyed to be put into a cage by the aid of the lifting conveying table 3 and the first conveyor 41. The carrying mechanism 2 is lifted and lowered in the designed channel of the goods shelf 5 until the goods shelf 5 is full of moulds. After the mould is filled, the first conveyor 41 conveys the pallet 5 out of the palletizing zone.
While the utility model has been described with reference to preferred embodiments, it is not intended to be limiting. Any person skilled in the art can make many possible variations and modifications to the technical solution of the present utility model or equivalent embodiments using the method and technical solution disclosed above without departing from the spirit and technical solution of the present utility model. Therefore, any simple modification, equivalent substitution, equivalent variation and modification of the above embodiments according to the technical substance of the present utility model, which do not depart from the technical solution of the present utility model, still fall within the scope of the technical solution of the present utility model.
Claims (10)
1. An apparatus for mold stacking, comprising: a lifting mechanism (1) and a bearing mechanism (2) for bearing the mould (6); the lifting mechanism (1) comprises a mounting bracket (11) and a first driving assembly (13); the mounting support (11) is arranged on the side of the conveyor (4), the bearing mechanism (2) is arranged on the mounting support (11), the output end of the first driving assembly (13) is connected with the bearing mechanism (2), and under the driving of the first driving assembly (13), the bearing mechanism (2) is lifted up and down reciprocally along the mounting support (11) and the inside of the goods shelf (5) so as to realize the stacking position preset on the goods shelf (5) from the stacking of the die (6).
2. Device for mould stacking according to claim 1, characterized in that the lifting mechanism (1) spans the ends of the adjacent conveyors (4) in a "gate" type structure.
3. Device for mould stacking according to claim 1, characterized in that a set of said lifting mechanisms (1) are symmetrically arranged on both sides of the conveyor (4) along the direction of travel of the conveyor (4), and that both sides of the conveyor (4) are provided with carrying mechanisms (2).
4. A device for mould stacking according to claim 2 or 3, characterized in that the carrying means (2) comprises a carrying table (21) and a second driving assembly (22), the carrying table (21) being provided with a roller (26), the second driving assembly (22) being adapted to drive the roller (26) in rotation for effecting the movement of the mould (6) on the carrying table (21).
5. The device for stacking molds according to claim 4, characterized in that said carrying table (21) is of a "in-line" configuration, said drum (26) being disposed outside the carrying table (21).
6. The device for mould stacking according to claim 4, characterized in that said carrying means (2) further comprise: a first mounting plate (23), a second mounting plate (24) and a first pulley (25); the bearing table (21) is arranged on the second mounting plate (24) and is used for bearing the die (6); the end of the first mounting plate (23) is connected with the second mounting plate (24), the first pulley (25) is mounted on the side of the second mounting plate (24), and the first pulley (25) slides back and forth along the inner side of the mounting bracket (11) under the driving of the first driving assembly (13) so as to realize the back and forth lifting of the bearing mechanism (2).
7. Device for mould stacking according to claim 4, characterized in that the carrying means (2) further comprise a lug (27), which lug (27) is located on the carrying table (21) or the first mounting plate (23) for connection to the first drive assembly (13).
8. The apparatus for mould stacking according to claim 6, characterized in that the lifting mechanism (1) further comprises a first guide rail (12); the first guide rail (12) is arranged on the inner side of the mounting bracket (11), the first pulley (25) is positioned in the first guide rail (12), and the first pulley (25) can lift and slide in a reciprocating manner along the first guide rail (12) under the driving of the first driving assembly (13).
9. The device for stacking molds according to any one of claims 5 to 7, wherein the lifting mechanism (1) further comprises a rotating shaft (14) and a pull rope (15), the output end of the first driving assembly (13) is connected with the rotating shaft (14), one end of the pull rope (15) is wound on the rotating shaft (14), the other end of the pull rope is connected with the bearing mechanism (2), and the pull rope (15) drives the bearing mechanism (2) to lift reciprocally along the mounting bracket (11) under the driving of the first driving assembly (13).
10. An automatic stacking system, characterized by comprising a device for mould stacking according to any one of claims 1 to 9, a conveyor (4) for conveying racks (5) and moulds (6) and a lifting conveyor (3) for lifting the conveyor (4) and moulds (6) to a preset stacking height, said device for mould stacking being arranged between adjacent conveyors (4) for assisting automatic stacking of moulds (6) into racks (5) on conveyors (4).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223598607.3U CN219155870U (en) | 2022-12-30 | 2022-12-30 | Device for mould stacking and automatic stacking system |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223598607.3U CN219155870U (en) | 2022-12-30 | 2022-12-30 | Device for mould stacking and automatic stacking system |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN219155870U true CN219155870U (en) | 2023-06-09 |
Family
ID=86638187
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202223598607.3U Active CN219155870U (en) | 2022-12-30 | 2022-12-30 | Device for mould stacking and automatic stacking system |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN219155870U (en) |
-
2022
- 2022-12-30 CN CN202223598607.3U patent/CN219155870U/en active Active
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110626700A (en) | Automated three-dimensional warehouse for pipes and its storage and storage methods | |
| CN212268732U (en) | Precise lifting, transfer and conveying device for stacking smoke boxes | |
| CN107098098B (en) | Shuttle car material case combined type lifting machine and shuttle garage | |
| CN211768039U (en) | Warehousing system | |
| CN209651121U (en) | A plate sorting and stacking machine | |
| CN216154991U (en) | Panel pile up neatly device | |
| CN113955503A (en) | Automatic tray conveying and stacking machine | |
| CN212832262U (en) | Lifting machine with circularly circulated trays | |
| CN212100626U (en) | Stepping type continuous elevator | |
| CN214455083U (en) | Full-automatic low-position stacker crane | |
| CN109205436A (en) | Multifunctional tray type vertical conveyor | |
| CN107792806B (en) | Concrete transportation scheduling device | |
| CN212638708U (en) | Automatic unloading equipment for three-dimensional warehouse delivery | |
| CN209905643U (en) | An automated storage system | |
| CN203558573U (en) | Pneumatic automatic brick hacking machine | |
| CN110683363A (en) | Lifting system is piled up to box | |
| CN209777569U (en) | A new energy storage vanadium battery stack production and transportation device | |
| CN217228906U (en) | Trolley layer-changing elevator | |
| CN110155737B (en) | Automatic leaning and unstacking system | |
| CN218859801U (en) | Mold stacking device and automatic stacking system | |
| CN219155871U (en) | Mould pile up neatly device and automatic pile up neatly system | |
| CN218859802U (en) | Device for die stacking and automatic stacking system | |
| CN219155889U (en) | Mould stacking device and automatic stacking system | |
| CN218200777U (en) | Automatic logistics conveying line | |
| CN216234910U (en) | Automatic tray conveying and stacking machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |