CN219026447U - Welding positioning tool for front panel of battery box body - Google Patents
Welding positioning tool for front panel of battery box body Download PDFInfo
- Publication number
- CN219026447U CN219026447U CN202222827555.6U CN202222827555U CN219026447U CN 219026447 U CN219026447 U CN 219026447U CN 202222827555 U CN202222827555 U CN 202222827555U CN 219026447 U CN219026447 U CN 219026447U
- Authority
- CN
- China
- Prior art keywords
- positioning
- long
- rod
- plate
- front panel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003466 welding Methods 0.000 title claims abstract description 27
- 230000001105 regulatory effect Effects 0.000 claims description 12
- 230000001276 controlling effect Effects 0.000 claims description 3
- 230000007547 defect Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Battery Mounting, Suspending (AREA)
Abstract
The utility model discloses a welding positioning tool for a front panel of a battery box body, which comprises the following steps: the long slat is fixedly provided with two handles; the two ends of the long slat are respectively provided with a first positioning block and two first positioning pins, the two ends of the two first positioning blocks are respectively provided with a first pin hole, and the two first positioning blocks are respectively fixed with the long slat; the two ends of the long slat are respectively provided with a second positioning block and a second positioning pin, the two second positioning blocks are respectively provided with a second pin hole, and the two second positioning blocks are respectively fixed with the long slat; the two sides of the long slat are respectively provided with a third positioning block and a third positioning pin, the two third positioning blocks are respectively provided with a third pin hole, and the two third positioning blocks are respectively fixed with the long slat; a plurality of propping rods are arranged at the rear of the long slat, and each propping rod is fixed with the long slat. The tool can rapidly and accurately position the front panel on the bottom plate of the battery box body without line drawing.
Description
Technical Field
The utility model relates to the field of production tools, in particular to a welding positioning tool for a front panel of a battery box body.
Background
The structure of battery box includes: the welding position of the front panel is usually determined by drawing lines on the port of the bottom plate by workers, and the front panel is positioned by drawing lines, so that the defects of low positioning efficiency and poor positioning precision exist.
Disclosure of Invention
The technical problems to be solved by the utility model are as follows: the welding positioning tool for the front panel of the battery box body is high in positioning efficiency and capable of accurately positioning the front panel.
In order to solve the problems, the utility model adopts the following technical scheme: battery box front panel welding position frock, its characterized in that: comprising the following steps: the front surface of the long strip plate is fixedly provided with two handles which are arranged side by side at intervals; the left end and the right end of the long slat are respectively provided with a first positioning block and two first positioning pins which run forwards and backwards, the front end and the rear end of the two first positioning blocks are respectively provided with a first pin hole, the two first positioning blocks are respectively fixed with the long slat through a first connecting frame, when the fixture is installed, the two first positioning blocks can be respectively placed on the left and right folded edges of the bottom plate of the battery box body, then each first pin hole on the two first positioning blocks can be respectively aligned up and down with a corresponding hole position on the folded edge of the bottom plate, and then the four first positioning pins can be respectively vertically inserted into the four first pin holes and the aligned hole positions on the folded edge of the bottom plate; the left end and the right end of the long slat are respectively provided with a second positioning block and a second positioning pin, the second positioning blocks are positioned at the rear of the long slat, the two second positioning blocks are respectively provided with a second pin hole, the lower surface of each second positioning block is provided with an opening for avoiding a nut on the front panel, and the two second positioning blocks are respectively fixed with the long slat through a second connecting frame; a third positioning block and a third positioning pin are respectively arranged on the upper rear parts of the left side and the right side of the long slat, the third positioning block is higher than the second positioning block, a third pin hole is respectively arranged on the two third positioning blocks, an opening for avoiding a nut on the front panel is arranged on the lower surface of each third positioning block, and the two third positioning blocks are respectively fixed with the long slat through a third connecting frame; the two second pin holes and the two third pin holes are arranged in left-right alignment; a plurality of abutting rods are arranged at the rear of the long slat at intervals along the long slat, each abutting rod is vertically arranged and aligned left and right, and each abutting rod is fixed with the long slat through a fourth connecting frame; when the front panel is positioned, each abutting rod can be used for abutting the front panel, two second positioning blocks can be respectively placed on the left end and the right end of the front panel, two third positioning blocks can be respectively placed on the left side and the right side of the top of the front panel, then two second pin holes and two third pin holes can be respectively aligned up and down with one hole position on the upper surface of the front panel, openings on the lower surfaces of the second positioning blocks and the third positioning blocks are used for avoiding nuts on hole positions, then two second positioning pins are respectively vertically inserted into the hole positions on the front panel aligned with the two second pin holes and the pin holes, and two third positioning pins are respectively vertically inserted into the hole positions on the front panel aligned with the two third pin holes and the pin holes, and then the front panel can be positioned on the bottom plate.
Further, the aforesaid battery box front panel welding position frock, wherein: the structure of first link includes: the first L-shaped rod is formed by vertically connecting a first long rod and a first short rod, the first long rod is arranged in a left-right trend, the first short rod is arranged in a front-back trend, the inner end of the first long rod is fixed with the front surface of the long plate, the outer end of the first long rod is connected with the rear end of the first short rod, a first connecting plate is arranged on the outer side of the first L-shaped rod, the first connecting plate is fixed with the outer side surface of the first short rod, a first positioning block is located below the first connecting plate, the first connecting plate is fixed with the middle of the first positioning block, a base plate is clamped between the first long rod and the long plate, the first connecting plate and the first short rod, the first connecting plate and the first positioning block are positioned by two pin rods, and the first positioning block is locked by screws.
Further, the aforesaid battery box front panel welding position frock, wherein: the structure of the second connecting frame comprises: the regulating block that is located the left and right sides trend of slat top, the regulating block is fixed mutually with the upper surface of slat, be provided with a second L shape pole at the rear of regulating block, the second L shape pole is by controlling the second stock that trend and the perpendicular second quarter butt that trend link to each other and constitute, the second stock is fixed mutually with the regulating block, the second locating piece is located the outside of second L shape pole, and fixed mutually with the second quarter butt, regulating block and slat, second stock and regulating block, all press from both sides between second locating piece and the second quarter butt and be equipped with the backing plate, adopt two round pin poles to fix a position, and adopt the screw to lock.
Further, the aforesaid battery box front panel welding position frock, wherein: the structure of the third connecting frame comprises: the third L-shaped rod and the fourth L-shaped rod are positioned above the long strip plate, the third L-shaped rod is formed by vertically connecting a left-right moving third long rod with a front-back moving third short rod, the fourth L-shaped rod is formed by vertically connecting a vertical moving fourth long rod with a front-back moving fourth short rod, the third long rod is fixed with the long strip plate, the third short rod is fixed with the fourth short rod, the third positioning block is positioned behind the fourth long rod and fixed with the fourth long rod, and a base plate is clamped between the third long rod and the long strip plate, between the third short rod and the fourth short rod, and between the third positioning block and the fourth long rod, and by using two pins for positioning and screws for locking.
Further, the aforesaid battery box front panel welding position frock, wherein: the structure of the fourth connecting frame comprises: the horizontal plate is horizontally arranged, the rear end of the horizontal plate is connected with the upper end of the vertical plate, the front end of the horizontal plate is fixed with the lower surface of the long plate, the abutting rod is located at the rear of the vertical plate, the abutting rod is fixed with the rear surface of the vertical plate, a base plate is clamped between the front end of the horizontal plate and the lower surface of the long plate, the abutting rod and the vertical plate, two pin rods are used for positioning, and screws are used for locking.
Further, the aforesaid battery box front panel welding position frock, wherein: each positioning pin is connected with the corresponding positioning block through a soft rope.
The utility model has the advantages that: the welding positioning tool for the front panel of the battery box body can rapidly and accurately position the front panel on the bottom plate of the battery box body without drawing lines by means of hole sites on the left and right folded sides of the bottom plate, so that the welding efficiency can be greatly improved.
Drawings
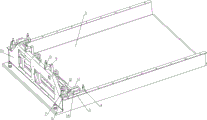
Fig. 1 is a schematic perspective view of a welding positioning tool for a front panel of a battery box body according to the present utility model.
Fig. 2 is a schematic perspective view of another view angle of the welding positioning tool for the front panel of the battery box body.
Fig. 3 is a schematic perspective view of a view angle of the welding positioning tool for the front panel of the battery box body.
Fig. 4 is a schematic perspective view of another view angle of the welding positioning tool for the front panel of the battery box body in the working process.
Detailed Description
The utility model is described in further detail below with reference to specific embodiments and the accompanying drawings.
As shown in fig. 1, 2, 3 and 4, the welding positioning tool for the front panel of the battery box body comprises: the long strip plate 1 which moves left and right is fixed with two handles 2 which are arranged side by side at intervals on the front surface of the long strip plate 1, and the tool can be conveniently lifted by the handles 2; the two ends of the long strip plate 1 are respectively provided with a first positioning block 3 and two first positioning pins 4 which move forwards and backwards, the front and rear ends of the two first positioning blocks 3 are respectively provided with a first pin hole, the two first positioning blocks 3 are respectively fixed with the long strip plate 1 through a first connecting frame, when the fixture is installed, the two first positioning blocks 3 can be respectively placed on the left and right two folds of the bottom plate 5 of the battery box body, then each first pin hole on the two first positioning blocks 3 can be respectively aligned up and down with one hole position on the fold of the bottom plate 5, and then the four first positioning pins 4 can be respectively vertically inserted into the four first pin holes and the holes on the fold of the bottom plate 5 aligned with the pin holes to position the fixture on the bottom plate 5; a second positioning block 6 and a second positioning pin 7 are respectively arranged at the left end and the right end of the long slat 1, the second positioning block 6 is positioned at the rear of the long slat 1, a second pin hole is respectively arranged on the two second positioning blocks 6, an opening 8 for avoiding a nut on the front panel 51 is arranged on the lower surface of each second positioning block 6, and the two second positioning blocks 6 are respectively fixed with the long slat 1 through a second connecting frame; a third positioning block 9 and a third positioning pin 10 are respectively arranged on the upper rear parts of the left side and the right side of the long slat 1, the third positioning block 9 is higher than the second positioning block 6, a third pin hole is respectively arranged on the two third positioning blocks 9, an opening 8 for avoiding nuts on the front panel 51 is arranged on the lower surface of each third positioning block 9, and the two third positioning blocks 9 are respectively fixed with the long slat 1 through a third connecting frame; each second pin hole and each third pin hole are arranged in left-right alignment; three abutting rods 11 are arranged at intervals along the long slat 1 side by side behind the long slat 1, each abutting rod 11 is vertically arranged and aligned left and right, and each abutting rod 11 is fixed with the long slat 1 through a fourth connecting frame; when the front panel 51 is positioned, each abutting rod 11 can be used for abutting the front panel 51, two second positioning blocks 6 can be respectively placed on the left end and the right end of the front panel 51, two third positioning blocks 9 can be respectively placed on the left side and the right side of the top of the front panel 51, then two second pin holes and two third pin holes can be respectively aligned up and down with one hole position on the upper surface of the front panel 51, openings 8 on the lower surfaces of the second positioning blocks 6 and the third positioning blocks 9 are used for avoiding nuts on hole positions, then two second positioning pins 7 are respectively vertically inserted into the hole positions on the front panel 51 aligned with the two second pin holes and the pin holes, and two third positioning pins 10 are respectively vertically inserted into the hole positions on the front panel 51 aligned with the two third pin holes and the pin holes, and then the front panel 51 can be positioned on the bottom plate 5.
In this embodiment, the structure of the first connecting frame includes: the first L-shaped rod is formed by vertically connecting a first long rod 12 and a first short rod 13, the first long rod 12 is arranged in a left-right trend, the first short rod 13 is arranged in a front-back trend, the inner end of the first long rod 12 is fixed with the front surface of the long slat 1, the outer end of the first long rod 12 is connected with the rear end of the first short rod 13, a first connecting plate 14 is arranged on the outer side of the first L-shaped rod, the first connecting plate 14 is fixed with the outer side surface of the first short rod 13, the first positioning block 3 is positioned below the first connecting plate 14, the first connecting plate 14 is fixed with the middle part of the first positioning block 3, and a backing plate is arranged between the first long rod 12 and the long slat 1, the first connecting plate 14 and the first short rod 13, and the first positioning block 14 and the first positioning block 3 in a clamping mode, positioning by adopting two pin rods and locking by adopting screws. The positions of the first positioning block 3 in front and back, left and right, up and down can be finely adjusted by changing the thickness of the backing plate.
The structure of the second connecting frame comprises: the adjusting block 15 that is located the left and right sides of lath 1 top trend, adjusting block 15 is fixed mutually with the upper surface of lath 1, be provided with a second L shape pole at the rear of adjusting block 15, the second L shape pole is by controlling the second stock 16 of trend and the perpendicular second quarter butt 17 of trend and link to each other and constitute, second stock 16 is fixed mutually with adjusting block 15, second locating piece 6 is located the outside of second L shape pole, and fix with second quarter butt 17, all press from both sides between adjusting block 15 and lath 1, second stock 16 and adjusting block 15, second locating piece 6 and second quarter butt 17 is equipped with the backing plate, adopt two round pin poles to fix a position, and adopt the screw to lock. The positions of the second positioning block 6 in front and back, left and right, up and down can be finely adjusted by changing the thickness of the backing plate.
The structure of the third connecting frame comprises: the third L-shaped rod and the fourth L-shaped rod are positioned above the long slat 1, the third L-shaped rod is formed by vertically connecting a third long rod 18 which runs left and right and a third short rod 19 which runs front and back, the fourth L-shaped rod is formed by vertically connecting a fourth long rod 20 which runs vertically and a fourth short rod 21 which runs front and back, the third long rod 18 is fixed with the long slat 1, the third short rod 19 is fixed with the fourth short rod 21, the third positioning block 9 is positioned behind the fourth long rod 20 and is fixed with the fourth long rod 20, and a base plate is arranged between the third long rod 18 and the long slat 1, between the third short rod 19 and the fourth short rod 21, and between the third positioning block 9 and the fourth long rod 20 for positioning by adopting two pin rods and locking by adopting screws. The positions of the third positioning block 9 in front and back, left and right, up and down can be finely adjusted by changing the thickness of the backing plate.
The structure of the fourth connecting frame comprises: the horizontal plate 22 and the vertical plate 23 are vertically arranged, the horizontal plate 22 is horizontally arranged, the rear end of the horizontal plate 22 is connected with the upper end of the vertical plate 23, the front end of the horizontal plate 22 is fixed with the lower surface of the long plate 1, the abutting rod 11 is positioned behind the vertical plate 23, the abutting rod 11 is fixed with the rear surface of the vertical plate 23, and a base plate is clamped between the front end of the horizontal plate 22 and the lower surface of the long plate 1, the abutting rod 11 and the vertical plate 23, two pin rods are used for positioning, and screws are used for locking. The position of the abutment bar 11 can be finely adjusted in the front-rear, up-down direction by changing the thickness of the pad.
In order to prevent the positioning pins from being lost, each positioning pin is connected with the corresponding positioning block through a soft rope, and the soft rope is not shown in the figure.
Before positioning, a welding positioning tool is placed on the bottom plate 5 in a crossing manner, two first positioning blocks 3 are placed on the left and right folded edges of the bottom plate 5 respectively, then each first pin hole on the two first positioning blocks 3 is aligned with a corresponding hole on the folded edge of the bottom plate 5 vertically respectively, and then four first positioning pins 4 are vertically inserted into the four first pin holes and the holes on the folded edge of the bottom plate 5 aligned with the pin holes respectively, so that the welding positioning tool can be positioned on the bottom plate 5; then, the front panel 51 is positioned, each abutting rod 11 is used for abutting the front panel 51, two second positioning blocks 6 are respectively placed on the left and right ends of the front panel 51, two third positioning blocks 9 are respectively placed on the left and right sides of the top of the front panel 51, then two second pin holes and two third pin holes are respectively aligned up and down with a corresponding hole on the upper surface of the front panel 51, openings 8 on the lower surfaces of the second positioning blocks 6 and the third positioning blocks 9 are used for avoiding nuts on hole sites, then two second positioning pins 7 are respectively vertically inserted into the hole sites on the front panel 51 aligned with the two second pin holes and the pin holes, and two third positioning pins 10 are respectively vertically inserted into the hole sites on the front panel 51 aligned with the two third pin holes and the pin holes, so that the front panel 51 can be rapidly and accurately positioned on the bottom plate 5.
Claims (6)
1. Battery box front panel welding position frock, its characterized in that: comprising the following steps: the front surface of the long strip plate is fixedly provided with two handles which are arranged side by side at intervals; the left end and the right end of the long slat are respectively provided with a first positioning block and two first positioning pins which run forwards and backwards, the front end and the rear end of the two first positioning blocks are respectively provided with a first pin hole, the two first positioning blocks are respectively fixed with the long slat through a first connecting frame, when the fixture is installed, the two first positioning blocks can be respectively placed on the left and right folded edges of the bottom plate of the battery box body, then each first pin hole on the two first positioning blocks can be respectively aligned up and down with a corresponding hole position on the folded edge of the bottom plate, and then the four first positioning pins can be respectively vertically inserted into the four first pin holes and the aligned hole positions on the folded edge of the bottom plate; the left end and the right end of the long slat are respectively provided with a second positioning block and a second positioning pin, the second positioning blocks are positioned at the rear of the long slat, the two second positioning blocks are respectively provided with a second pin hole, the lower surface of each second positioning block is provided with an opening for avoiding a nut on the front panel, and the two second positioning blocks are respectively fixed with the long slat through a second connecting frame; a third positioning block and a third positioning pin are respectively arranged on the upper rear parts of the left side and the right side of the long slat, the third positioning block is higher than the second positioning block, a third pin hole is respectively arranged on the two third positioning blocks, an opening for avoiding a nut on the front panel is arranged on the lower surface of each third positioning block, and the two third positioning blocks are respectively fixed with the long slat through a third connecting frame; the two second pin holes and the two third pin holes are arranged in left-right alignment; a plurality of abutting rods are arranged at the rear of the long slat at intervals along the long slat, each abutting rod is vertically arranged and aligned left and right, and each abutting rod is fixed with the long slat through a fourth connecting frame; when the front panel is positioned, each abutting rod can be used for abutting the front panel, two second positioning blocks can be respectively placed on the left end and the right end of the front panel, two third positioning blocks can be respectively placed on the left side and the right side of the top of the front panel, then two second pin holes and two third pin holes can be respectively aligned up and down with one hole position on the upper surface of the front panel, openings on the lower surfaces of the second positioning blocks and the third positioning blocks are used for avoiding nuts on hole positions, then two second positioning pins are respectively vertically inserted into the hole positions on the front panel aligned with the two second pin holes and the pin holes, and two third positioning pins are respectively vertically inserted into the hole positions on the front panel aligned with the two third pin holes and the pin holes, and then the front panel can be positioned on the bottom plate.
2. The battery box body front panel welding positioning tool according to claim 1, wherein: the structure of first link includes: the first L-shaped rod is formed by vertically connecting a first long rod and a first short rod, the first long rod is arranged in a left-right trend, the first short rod is arranged in a front-back trend, the inner end of the first long rod is fixed with the front surface of the long plate, the outer end of the first long rod is connected with the rear end of the first short rod, a first connecting plate is arranged on the outer side of the first L-shaped rod, the first connecting plate is fixed with the outer side surface of the first short rod, a first positioning block is located below the first connecting plate, the first connecting plate is fixed with the middle of the first positioning block, a base plate is clamped between the first long rod and the long plate, the first connecting plate and the first short rod, the first connecting plate and the first positioning block are positioned by two pin rods, and the first positioning block is locked by screws.
3. The battery box body front panel welding positioning tool according to claim 1, wherein: the structure of the second connecting frame comprises: the regulating block that is located the left and right sides trend of slat top, the regulating block is fixed mutually with the upper surface of slat, be provided with a second L shape pole at the rear of regulating block, the second L shape pole is by controlling the second stock that trend and the perpendicular second quarter butt that trend link to each other and constitute, the second stock is fixed mutually with the regulating block, the second locating piece is located the outside of second L shape pole, and fixed mutually with the second quarter butt, regulating block and slat, second stock and regulating block, all press from both sides between second locating piece and the second quarter butt and be equipped with the backing plate, adopt two round pin poles to fix a position, and adopt the screw to lock.
4. The battery box body front panel welding positioning tool according to claim 1, wherein: the structure of the third connecting frame comprises: the third L-shaped rod and the fourth L-shaped rod are positioned above the long strip plate, the third L-shaped rod is formed by vertically connecting a left-right moving third long rod with a front-back moving third short rod, the fourth L-shaped rod is formed by vertically connecting a vertical moving fourth long rod with a front-back moving fourth short rod, the third long rod is fixed with the long strip plate, the third short rod is fixed with the fourth short rod, the third positioning block is positioned behind the fourth long rod and fixed with the fourth long rod, and a base plate is clamped between the third long rod and the long strip plate, between the third short rod and the fourth short rod, and between the third positioning block and the fourth long rod, and by using two pins for positioning and screws for locking.
5. The battery box body front panel welding positioning tool according to claim 1, wherein: the structure of the fourth connecting frame comprises: the horizontal plate is horizontally arranged, the rear end of the horizontal plate is connected with the upper end of the vertical plate, the front end of the horizontal plate is fixed with the lower surface of the long plate, the propping rod is located at the rear of the vertical plate, the propping rod is fixed with the rear surface of the vertical plate, a base plate is clamped between the front end of the horizontal plate and the lower surface of the long plate, the propping rod and the vertical plate, two pin rods are used for positioning, and screws are used for locking.
6. The battery box body front panel welding positioning tool according to claim 1 or 2 or 3 or 4 or 5, wherein: each positioning pin is connected with the corresponding positioning block through a soft rope.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222827555.6U CN219026447U (en) | 2022-10-26 | 2022-10-26 | Welding positioning tool for front panel of battery box body |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222827555.6U CN219026447U (en) | 2022-10-26 | 2022-10-26 | Welding positioning tool for front panel of battery box body |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN219026447U true CN219026447U (en) | 2023-05-16 |
Family
ID=86291018
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202222827555.6U Active CN219026447U (en) | 2022-10-26 | 2022-10-26 | Welding positioning tool for front panel of battery box body |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN219026447U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119457667A (en) * | 2024-12-30 | 2025-02-18 | 江苏固铝科技有限公司 | Energy storage battery liquid cooling box welding clamping tooling |
-
2022
- 2022-10-26 CN CN202222827555.6U patent/CN219026447U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119457667A (en) * | 2024-12-30 | 2025-02-18 | 江苏固铝科技有限公司 | Energy storage battery liquid cooling box welding clamping tooling |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN115365826B (en) | Battery box body punching and welding positioning clamping combined tool | |
| CN210849315U (en) | A workpiece self-positioning clamping device for CNC milling machine | |
| CN219026448U (en) | Welding positioning tool for rear beam of battery box body | |
| CN219901179U (en) | Profiling limiting tool | |
| CN221185307U (en) | Welding equipment for skirt board of square pile | |
| CN218197473U (en) | A printing jig for a printing machine | |
| CN220178725U (en) | Milling machine fixture for mining machinery manufacturing | |
| CN218874059U (en) | Multi-functional protection frock of welding plate back | |
| CN208067829U (en) | A kind of frock clamp for processing locking bar positioning inclined-plane | |
| CN110877180A (en) | Sheet metal welding fixture replacing device | |
| CN113732374B (en) | Steel structure plate milling equipment | |
| CN212959693U (en) | Belt connecting machine | |
| CN212793741U (en) | Flexible tool positioning base | |
| CN221502665U (en) | A clamp with adjustable width | |
| CN111843356B (en) | Welding fixture for transformer box body | |
| CN220863926U (en) | Multipurpose workbench assembling module | |
| CN223917291U (en) | Small excavator movable arm integrated machining tool | |
| CN218193463U (en) | Spot welding tool for upper bracket of front oil cylinder of commercial vehicle | |
| CN222020938U (en) | A universal welding tool for profile flatness | |
| CN220636817U (en) | Cab bottom plate tailor-welded tooling | |
| CN223701134U (en) | A multi-station workbench for drilling holes in sword hilts | |
| CN222569712U (en) | Auxiliary welding tool for milling machine frame production | |
| CN206405742U (en) | A kind of hole drilling jig | |
| CN221539578U (en) | Positioning tool for automobile connecting seat | |
| CN222986062U (en) | A door frame welding tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address | ||
| CP03 | Change of name, title or address |
Address after: No. 6 Dongli Road, Yangshe Town, Zhangjiagang City, Suzhou City, Jiangsu Province, 215600 Patentee after: Jiangsu Gulu Technology Co.,Ltd. Address before: 215600 Zhangjiagang solid aluminum metal products Co., Ltd., xizha village, yangshe Town, Suzhou City, Jiangsu Province Patentee before: Zhangjiagang solid aluminum metal products Co.,Ltd. |