CN219004299U - Cutting-off type stamping die - Google Patents
Cutting-off type stamping die Download PDFInfo
- Publication number
- CN219004299U CN219004299U CN202223568490.4U CN202223568490U CN219004299U CN 219004299 U CN219004299 U CN 219004299U CN 202223568490 U CN202223568490 U CN 202223568490U CN 219004299 U CN219004299 U CN 219004299U
- Authority
- CN
- China
- Prior art keywords
- plate
- die
- lower bolster
- die holder
- cutting
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 239000000463 material Substances 0.000 claims abstract description 73
- 238000005520 cutting process Methods 0.000 claims abstract description 13
- 238000004080 punching Methods 0.000 claims abstract description 10
- 238000000034 method Methods 0.000 abstract description 12
- 238000004519 manufacturing process Methods 0.000 abstract description 3
- 229910000831 Steel Inorganic materials 0.000 description 4
- 238000007599 discharging Methods 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- 230000006835 compression Effects 0.000 description 2
- 238000007906 compression Methods 0.000 description 2
- 230000008092 positive effect Effects 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000003672 processing method Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
Images



Landscapes
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
Abstract
The utility model provides a cutting-off type stamping die, which solves the problems of low stamping efficiency caused by long time of manual operators due to two working procedures of blanking and punching when the existing stamping die works, and adopts the following technical scheme: the upper template lower part has set gradually the upper padding plate, the punch's punch holder and has gone up the take off the board, is provided with the lower bolster between lower bolster and the die holder, and the die holder discharge end is provided with the material that utilizes the spring to prop up the material, and the material piece discharge end is connected with the locating plate that has the reference column, and the die holder is provided with the mould stop screw that is useful to restrict material piece movable range, and the lower bolster is provided with spacing post and punching press hole, and the front end that the lower bolster pressed close to the material is provided with the lower bolster sword blade that is used for cutting off the material. The device has reasonable structure, is convenient for continuous work, saves working procedure time and labor, and improves production efficiency and material utilization rate.
Description
Technical Field
The utility model relates to the technical field of stamping dies, in particular to a cutting-off type stamping die which is used for stamping and manufacturing steel coils and strips.
Background
The stamping is a forming processing method for obtaining a workpiece with a required shape and size by applying external force to plates, strips, pipes, sectional materials and the like by using a press machine and a die to enable the plates, the strips, the pipes, the sectional materials and the like to generate plastic deformation or separation. In prior art, stamping die body is including the cope match-plate pattern of connecting the press and set up the lower bolster on the platform, when stamping working to coil of strip material, adopts blanking and twice processes of punching a hole generally, can not continuous operation, and manual operation has increased process time, causes stamping efficiency low.
Disclosure of Invention
The utility model aims to provide a cutting-off type stamping die, which solves the problems of low stamping efficiency caused by the time length of a manual operator because the blanking and punching processes are needed during working of the conventional stamping die, has reasonable structure, is convenient for continuous working, saves the process time and labor, and improves the production efficiency and the utilization rate of materials.
The technical scheme adopted by the utility model is as follows: the cutting-off type stamping die comprises a stamping die body, wherein the stamping die body is provided with an upper die plate connected with a press machine and a lower die plate arranged on a lower die base, and the technical key points are that: the upper template lower part has set gradually the upper padding plate, has been provided with punch's punch holder and has gone up the stripper, is provided with the lower bolster between lower bolster and the die holder, and the die holder discharge end is provided with the material that utilizes the spring to prop up the material, and the material piece discharge end is connected with the locating plate that has the reference column, and the die holder is provided with the mould stop screw that is used for restricting material piece movable range, and the lower bolster is provided with spacing post and punching press hole, and the front end that the lower bolster pressed close to the material is provided with the lower bolster sword blade that is used for cutting off the material.
The limiting columns are symmetrically arranged on two sides of the lower die plate, the positioning columns are arranged on two sides and the front end of the positioning plate, and equal-height material plate guide sliding grooves are formed in the inner sides of the limiting columns and the positioning columns on two sides of the positioning plate.
The utility model has the advantages and positive effects that: the cutting-off type stamping die adopts the structure that the upper base plate, the upper clamping plate provided with the punch and the upper stripper plate are sequentially arranged at the lower part of the upper die plate, the lower base plate is arranged between the lower die plate and the lower die holder, and the lower die plate is provided with the limiting column and the stamping hole, so that the material can be conveniently and rapidly stamped; because the material floating block which utilizes the spring to prop up the material is arranged at the discharging end of the lower die holder, the positioning plate with the positioning column is connected at the discharging end of the material floating block, the die stop screw which is used for limiting the moving range of the material floating block is arranged at the lower die holder, and the cutting edge for cutting off the material is arranged at the front end of the lower die plate, which is close to the material floating block, so that the material can be pushed forward to the next step after being stamped, the material can be directly cut off by utilizing the elastic support and fall-back of the material floating block through the cutting edge of the lower die, and continuous stamping and cutting-off procedure is formed.
Drawings
The utility model is further described below with reference to the accompanying drawings.
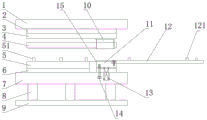
FIG. 1 is a schematic overall structure of an embodiment of the present utility model;
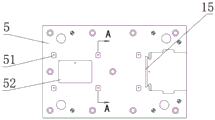
FIG. 2 is a schematic view of the structure of the lower die plate of the present utility model;
FIG. 3 is a cross-sectional view taken along A-A of FIG. 2;
FIG. 4 is a schematic view of the structure of the lower mat of the present utility model;
FIG. 5 is a schematic view of a positioning plate structure of the present utility model;
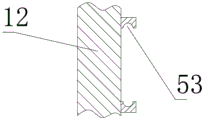
FIG. 6 is a B-B cross-sectional view of FIG. 5;
fig. 7 is a schematic view of the blanking use state of the present utility model.
The serial numbers in the figures illustrate: the die comprises an upper die plate 1, an upper base plate 2, an upper clamping plate 3, an upper stripper plate 4, a lower die plate 5, a lower base plate 6, a lower die holder 7, a lower cushion block 8, a lower supporting plate 9, a punch 10, a float block 11, a positioning block 12, a spring 13, a die stop screw 14, a die cutting edge 15, a material 20, a material 21 rear section, a material 22 front section, a 51 limit column, a 52 punching hole, a 53 guide chute and a 121 positioning column.
Detailed Description
Referring to fig. 1 to 7, which illustrate the specific structure of the present utility model in detail, an embodiment of the present utility model is shown in fig. 1, and a cut-off type stamping die comprises a stamping die body assembled with an upper die plate 1 connected to a press machine and a lower die plate 5 provided on a lower die holder 7, wherein an upper pad plate 2, an upper clamping plate 3 provided with a punch 10 and an upper stripper plate 4 are sequentially provided on the lower portion of the upper die plate 1, wherein the upper die plate 1 is made of 45 # steel material for fixing the upper clamping plate 3 and the upper pad plate 2 together, and carrying the blanking force transmitted by the upper pad plate during the stamping of the die; the upper base plate 2 is made of Cr12MoV material and bears the acting force of the punch of the upper clamping plate, so that the elastic element is ensured to have enough compression distance; the hardness of the upper die holder is smaller than that of the upper base plate, so that the upper die holder is protected; the upper clamping plate 3 is made of 45 # steel, the punch 10 is fixed, the position of the punch is ensured, and the elastic element is ensured to have enough compression distance; the upper stripper plate 4 is made of Cr12MoV material, and is guided by a punch and used for pressing and stripping. A lower base plate 6 is arranged between the lower die plate 5 and the lower die base 7, the lower die plate 5 and the lower base plate 6 are combined into an integral structure, a lower cushion block 8 and a lower supporting plate 9 are arranged below the lower die base 7, a floating block 11 supported by a spring 13 is arranged at the discharge end of the lower die base 7, a positioning plate 12 is connected at the discharge end of the floating block, and a positioning column 121 is arranged on the positioning plate 12 as shown in fig. 5. The lower die holder 7 is provided with a die stop screw 14 for limiting the movable range of the float block 11, as shown in fig. 2, the lower die plate 5 is provided with a limit post 51 and a punching hole 52, and the front end of the lower die plate 5 close to the float block is provided with a lower die plate knife edge for cutting off materials. The lower template 5 is made of Cr12MoV material and is used for fixing the cutting edge of a lower template cutter so as to ensure the position of the cutter edge; as shown in fig. 4, the lower base plate 6 is made of Cr12MoV material and is used for bearing the impact force of the punching of the upper edge of the lower template, the hardness of the lower die base is smaller than that of the lower base plate, and the lower base plate also protects the lower die base; the lower die holder 7 is made of 45 # steel material, and a lower base plate and a lower die plate are fixed together; carrying the blanking force transmitted by the upper backing plate during the stamping of the die; the lower supporting plate 9 is used for clamping the die and the working table of the press. The float block 11 is made of Cr12MoV material and is used for supporting the material belt upwards; the spring 13 plays a role in material returning after stamping; the die stop screw is also used for controlling die fittings of the die opening stroke between the lower die plate, the lower base plate and the lower die base.
As shown in fig. 3 and 6, as a further improvement, the limiting columns 51 are symmetrically arranged at two sides of the lower template 5, the positioning columns 121 are arranged at two sides and the front end of the positioning plate 12, and the inner sides of the positioning columns at two sides of the limiting columns and the positioning plate are provided with the material plate guiding sliding grooves 53 with equal height, so that the materials can be positioned rapidly and accurately.
The working principle and the using method are as follows: as shown in fig. 7, when the cutting-off type stamping die works, strip-shaped materials 20 are guided and fed into the positioning plate 12 through the limiting columns 51, when the upper die plate 1 descends along with the sliding block, the upper stripper plate 4 firstly presses the materials to move downwards against the floating material block 11 until the materials 20 contact with the cutting edge 15 of the lower die plate to cut off the materials, at the moment, the materials form a material rear section 21 in a stamping state and a material front section 22 clamped between the upper die plate and the floating material block, and when the upper die plate ascends, the material front section is ejected out of the lower die plate by the floating material block through the elasticity of the spring; meanwhile, the movable range of the floating block is limited by the die stop screw, and the cut-off material workpiece is taken away, so that the whole blanking process is completed. And then the strip-shaped material is fed into a step distance to carry out the next blanking and punching process, and the process is carried out repeatedly. The cutting-off type stamping die adopts the structure that the upper base plate, the upper clamping plate provided with the punch and the upper stripper plate are sequentially arranged at the lower part of the upper die plate, the lower base plate is arranged between the lower die plate and the lower die holder, and the lower die plate is provided with the limiting column and the stamping hole, so that the material can be conveniently and rapidly stamped; because the material floating block which utilizes the spring to prop up the material is arranged at the discharging end of the lower die holder, the positioning plate with the positioning column is connected at the discharging end of the material floating block, the die stop screw which is used for limiting the moving range of the material floating block is arranged at the lower die holder, and the cutting edge for cutting off the material is arranged at the front end of the lower die plate, which is close to the material floating block, so that the material can be pushed forward to the next step after being stamped, the material can be directly cut off by utilizing the elastic support and fall-back of the material floating block through the cutting edge of the lower die, and continuous stamping and cutting-off procedure is formed.
In view of the above, the object of the present utility model is achieved.
Claims (2)
1. The utility model provides a cut-off stamping die, includes the stamping die body of the cope match-plate pattern and the lower bolster of setting on the die holder of assembly connection press, its characterized in that: the upper template lower part has set gradually the upper padding plate, has been provided with punch's punch holder and has gone up the stripper, is provided with the lower bolster between lower bolster and the die holder, and the die holder discharge end is provided with the material that utilizes the spring to prop up the material, and the material piece discharge end is connected with the locating plate that has the reference column, and the die holder is provided with the mould stop screw that is used for restricting material piece movable range, and the lower bolster is provided with spacing post and punching press hole, and the front end that the lower bolster pressed close to the material is provided with the lower bolster sword blade that is used for cutting off the material.
2. The cutoff stamping die as recited in claim 1, wherein: the limiting columns are symmetrically arranged on two sides of the lower die plate, the positioning columns are arranged on two sides and the front end of the positioning plate, and equal-height material plate guide sliding grooves are formed in the inner sides of the limiting columns and the positioning columns on two sides of the positioning plate.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223568490.4U CN219004299U (en) | 2022-12-31 | 2022-12-31 | Cutting-off type stamping die |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223568490.4U CN219004299U (en) | 2022-12-31 | 2022-12-31 | Cutting-off type stamping die |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN219004299U true CN219004299U (en) | 2023-05-12 |
Family
ID=86234035
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202223568490.4U Active CN219004299U (en) | 2022-12-31 | 2022-12-31 | Cutting-off type stamping die |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN219004299U (en) |
-
2022
- 2022-12-31 CN CN202223568490.4U patent/CN219004299U/en active Active
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109500242A (en) | A kind of many types of face processing and forming stamping die of vehicle dormer window guide rail and its process for stamping | |
| CN114011950B (en) | Middle-channel stamping forming die for left and right parts of automobile A column | |
| CN213530434U (en) | Automatic forming and stamping die for upper cover plate of quick-release lock part | |
| CN216780043U (en) | Stamping die | |
| CN208408175U (en) | Vertical and lateral one-shot forming dies | |
| CN205629097U (en) | Reverse tensile lid upgrades mould | |
| CN209986083U (en) | Stamping die for notebook computer keyboard frame | |
| CN221817165U (en) | Stretching stepping die for movable castor support | |
| CN202861132U (en) | Welding test piece mould | |
| CN214133585U (en) | Automatic forming stamping die for elastic sheet on quick-release lock part | |
| CN216857927U (en) | Product side blow mechanism | |
| CN114309248B (en) | Continuous forming die for processing corrugated resistor tube support | |
| CN212822074U (en) | Double-notch cutting device for stamping U-shaped guide groove piece | |
| CN213671449U (en) | Combined stretching die | |
| CN111545691B (en) | A kind of semi-open metal elastic part forming equipment and forming method thereof | |
| CN209969352U (en) | Deep-drawing and edge-extruding composite die | |
| CN222856491U (en) | Production die for automobile parts | |
| CN213052331U (en) | Punching conjoined die | |
| CN218340864U (en) | Demoulding device of stamping die | |
| CN216881332U (en) | Punching device for child seat support | |
| CN213915751U (en) | High-precision bending die | |
| CN224168516U (en) | A stamping die for an air compressor switch cover | |
| CN218574758U (en) | Stamping die with synchronous side punching and hole flanging | |
| CN223197847U (en) | A pin terminal piercing and blanking structure | |
| CN222902374U (en) | Stamping die for shock mount |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |